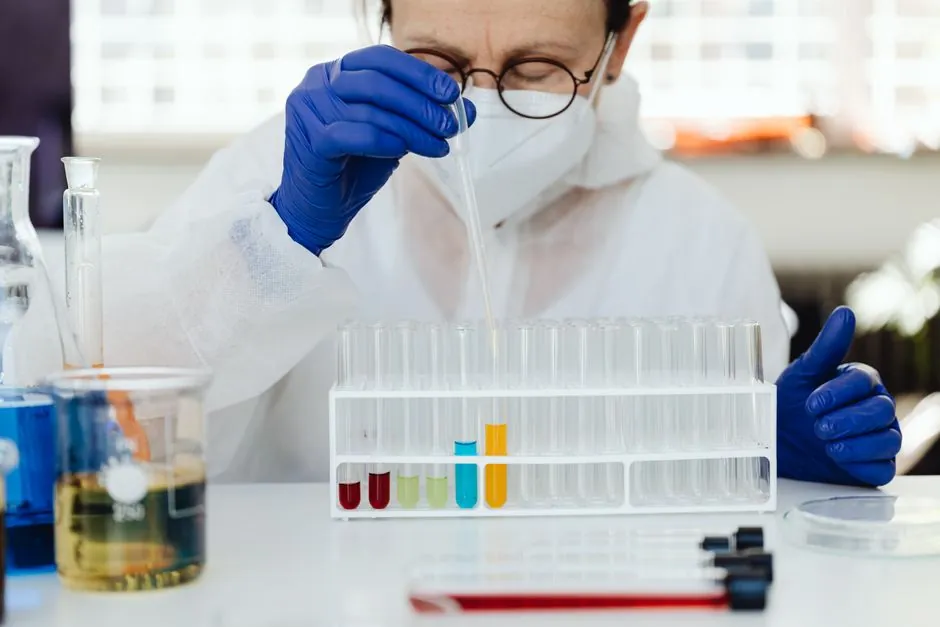
Glass tube variable area flowmeters and metal tube variable area flowmeters are the same instrument family differentiated by tube material, with direct consequences for accuracy, pressure rating, output capability, and unit cost [S2][S3].
Both designs use a tapered tube and a free-moving float: as flow increases, the float rises until upward fluid drag balances float weight, and the float position on a graduated scale indicates flow rate [S5]. Material choice is the decision point, not operating principle.
Operating Envelope: Borosilicate Glass vs Stainless/Brass Metal
Glass tube rotameters are built around a precision-formed borosilicate glass tube with floats of glass, plastic, or stainless steel, and are typically used at low to medium temperature and pressure on clean liquids and gases [S5][S6]. The fundamental limit is the brittleness of the glass envelope; metal tube rotameters replace that envelope with stainless steel, aluminum, or brass, extending the operating range to high temperature, high pressure, steam, and corrosive media [S2][S3].
For applications where temperature or pressure exceeds what a glass tube can survive, a metal tube rotameter with local indication is the standard fallback, and where remote electrical output is required, the metal tube design is essentially mandatory because the opaque tube rules out visual reading [S3]. The trade-off is unit cost: glass is the cheapest local indicator, metal is a step up but still a fraction of a Coriolis or magnetic meter at the same line size [S1][S3].
Accuracy, Output, and Integration
Typical rotameter accuracy sits in the 1-5% of full scale range, and glass tube meters in particular are not specified above roughly 1.5% FS; for crude oil custody transfer or any application needing 0.2-0.5% FS, neither glass nor metal rotameter is appropriate, and a positive displacement or Coriolis meter must be used [S3][S4].
Glass rotameters generally do not provide an electrical output, which makes them a pure local indicator, while metal tube rotameters almost always include a magnetic follower that drives a 4-20mA, HART, or pulse output for SCADA, totalization, and closed-loop flow control [S1][S2][S7]. This is the single biggest reason process plants standardize on metal tube rotameters for anything beyond a sight glass on a utility header.
Media Compatibility and Float Selection
Float material is matched to the wetted process: glass, plastic (PVC, PTFE), or stainless steel floats in a glass tube for water, air, and mild chemicals; stainless steel, Hastelloy, PTFE-lined, or other alloy floats in a metal tube for acids, alkalis, hydrocarbons, and steam [S3][S5][S7]. For gas service specifically, models with guide rods or ribbed guiding structures inside the tapered tube are recommended to prevent the float from oscillating laterally and impacting the tube wall, a known failure mode in unguided glass tube gas rotameters [S3].
Single-phase clean liquids and gases are the primary measurement target; liquids carrying solids, gases with entrained droplets, or services where deposits can build on the float are unsuitable, and even a sub-visible coating on the float in a micro-flow meter can shift the reading by several percent over time [S3]. For those services, neither glass nor metal rotameter is the right tool, regardless of tube choice.
Selection Criteria Matrix
Five decision criteria separate the two variants cleanly: pressure/temperature rating, output type, media compatibility, accuracy ceiling, and unit cost. Glass wins on cost and direct visual reading; metal wins on pressure, temperature, opacity-tolerant fluids, and electrical output [S1][S2][S3][S7].
A direct comparison on the criteria that actually drive a purchase order:
Pressure/temperature rating: glass is limited to low-to-medium service (typically a few bar and below roughly 150 degC depending on cone size); metal tube extends to high pressure steam and process temperatures well beyond that envelope [S2][S3][S5].
Output: glass is local visual only with no electrical output as a rule; metal provides 4-20mA, HART, or pulse for remote integration and totalization [S1][S2][S7].
Media: glass suits clean water, air, and mild chemicals; metal suits steam, corrosive acids/alkalis, opaque hydrocarbons, and aggressive process fluids when paired with the correct float and lining material [S3][S5][S7].
Accuracy: both are in the 1-5% FS band, with glass typically not specified finer than 1.5% FS; neither meets sub-1% custody-transfer requirements [S3][S4].
Cost: glass is the lowest-cost local indicator; metal is a moderate step up but remains inexpensive relative to Coriolis, ultrasonic, or variable area flowmeter electronic alternatives with comparable output [S1][S3].
Use Cases: Where Each Design Fits
Glass tube rotameters remain the default for laboratory bench flow indication, analytical instrument purge meters, HVAC chilled-water headers, water-treatment chemical dosing skids where the operator wants to see the float, and any cost-sensitive local-indication service below the glass pressure/temperature ceiling [S2][S3][S5].
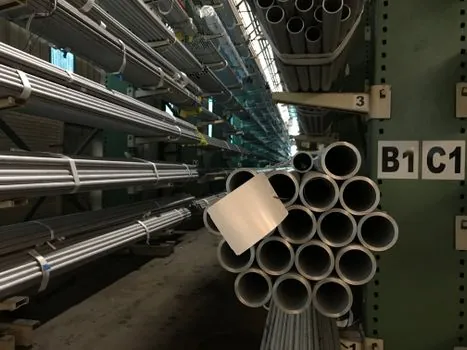
Metal tube rotameters are specified for steam flow on boilers and heat exchangers, oil and gas purge and chemical injection lines, chemical processing acid and alkali services, pharmaceutical bioreactor feed, power plant cooling water monitoring, and any application requiring 4-20mA or HART output to a DCS for totalization, trending, or closed-loop control [S2][S3][S7]. For threshold-only high/low flow alarms, a simple metal tube rotameter with a limit switch is often the lowest-cost reliable solution [S3].
Installation, Safety, and Failure Modes
Glass rotameters must be installed vertically on a vibration-free pipe with the inlet connected to the small (bottom) end of the cone, and the connected piping must be firmly supported so no mechanical stress is transferred to the glass tube [S1]. A transparent protective splash guard is recommended on every glass rotameter to contain fluid release on tube rupture and buy time for emergency isolation [S3].
Verification media must be clean, an upstream filter is required for dirty services, and gas calibration requires a thermometer with 0.2 degC minimum division plus a pressure gauge accurate to within +/-1% near the inlet [S1]. The main failure modes are float clogging on dirty service, float wear in abrasive slurries, glass tube rupture on mechanical impact or thermal shock, and calibration drift on viscous fluids where the indicated flow diverges from the actual flow unless the meter was wet-calibrated at process conditions [S1][S3].
Sourcing, Standards, and Specifying
Specifying engineers should request calibration media, calibration temperature and pressure, full-scale flow, wetted material list (tube, float, seals, linings), output type, process connection size and rating, and the maximum working pressure and temperature on the nameplate or calibration certificate [S1][S3]. A flow standard device used to verify the meter must itself carry a valid verification certificate and be at least twice as accurate as the meter under test [S1].
For hazardous-area service, metal tube rotameters with appropriate certifications are specified, and where only a pneumatic control system is available in an explosive environment, pneumatic transmission is preferred over electronic output [S3]. Procurement should also confirm the float material is compatible with the process fluid at the design temperature, since a stainless float that works on water at 25 degC may pit badly on a hot chloride service.
Trackable signals to watch over the next procurement cycle: vendor moves toward HART 7 and IO-Link output on metal tube rotameters, wider adoption of PTFE and Hastelloy linings for aggressive chemical service, and continued price compression on electronic variable area flowmeter replacements from Chinese OEMs offering 4-20mA metal tube units at glass-tube price points.
Component reference pages worth checking: metal material, and metal powder.
This topic is covered further in When Guard Locking Is Required: Stopping Time vs Access Time per ISO 14119.