A cooler-mixer that folds evaporative air cooling into the muller cycle can replace a separate sand cooler for green return sand, provided shakeout temperature stays below about 100°C and the sand-to-metal ratio is high enough that 3% residual moisture is available for flash evaporation [S1].
The choice is not binary between technologies but between two duty envelopes: the continuous, high-throughput cooler (rotary drum, fluid bed, or water-tube MD cooler) sized in tph, and the batch cooler-muller where the same pan handles homogenization, water addition, and air cooling in one cycle [S3][S4].
Sand temperature at shakeout drives the decision
Return sand arriving at the cooling stage sets the duty. In a 5:1 sand-to-metal ratio line, shakeout sand regularly runs 165°C (330°F) at the discharge, while a high-ratio shop with adequate moisture in the return stream can land closer to 100°C (212°F) and skip the flash-cooling water-addition step entirely [S1].
The threshold that matters is whether the moisture already present in the return sand is sufficient to drive evaporation. A staged approach adds water to sand hotter than 100°C, lets a fraction flash to steam, and lands the bed near 95°C (203°F) before the residual 3% moisture finishes the drop across subsequent stages [S1]. A cooler-muller that does its own water metering cannot recover that much delta-T in a single batch without extending cycle time well past typical 90-180 second mulling windows.
Three options for moving heat out of return sand
Three cooler architectures show up in current foundry specification: rotary blending/cooling drums, vibrating fluid beds, and integrated cooler-mullers. Each handles a different slice of the duty envelope. A fluidized bed cooler, like Carrier's drilled-deck design or the Vulcan V-Cooler mounted on the return belt, can run as a continuous device with no moving parts in contact with the sand and uses controlled water addition plus vibration to eliminate hot spots [S2][S4]. A water-cooled MD Cooler (sizes 454 through 754) drops heat through finned tubes, a fit for plants that already run a chilled-water loop and want to avoid adding dust-handling to the cooling stage [S4].
Where the integrated path wins is on footprint and binder efficiency. The Scoval Maxcool adds a distributor, air injection pipes, and a centrifugal fan to a standard Rotomax muller pan, and uses cycle-start measurements of sand mass, sand temperature, air temperature, and humidity to size water addition and cooling time per batch [S3]. Because the sand is humidified before the air register opens, fines (bentonite and coal dust) stay in the bed rather than reporting to the air stream, a problem that plagues continuous air-only coolers [S3]. The same vendor lists the result as simplified sand plant layout, reduced power draw, improved flowability and permeability, easier knockout, and lower water consumption [S3].
A separate Eirich air-cooling prep system targets the same homogenization plus cooling goal but keeps the mixing and cooling functions discrete, accepting the larger footprint to gain flexibility on binder distribution and cycle timing [S5]. The Sinto G-Cooler, a fluidized-bed reclamation cooler, sits at the cooler end of the spectrum and can be supplied with or without integrated heat-recovery [S7].
Air demand and energy: the sizing math
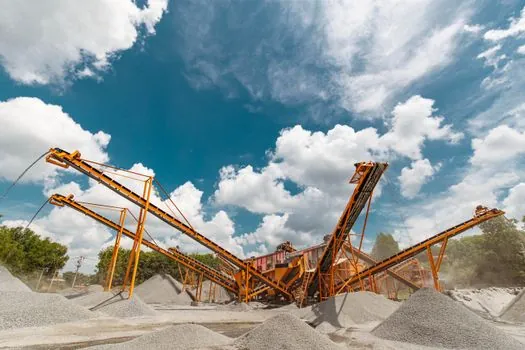
The rotary drum route, run as the third stage of a 100 tph three-stage system, needs 12,000 cfm of air to land a 40°C (70°F) delta-T, which works out to 33,500 joules per metric ton of sand or 317,000 Btu removed per ton [S1]. The rule of thumb from that same design envelope: 100 cfm per ton per hour of sand [S1]. At 5:1 sand-to-metal, that is roughly 20 tph of sand per ton of cast poured per hour, so a 10 tph casting line is already a 100 tph cooling duty before any margin is added.
A batch cooler-muller cannot match that throughput per machine because the cooling happens inside the mulling window. Throughput per cycle is bounded by pan diameter and sand depth, and the cycle only cools as fast as the air flow through the pan allows. That is why the integrated unit shows up in iron, steel, aluminum, and bronze foundries with modest tonnage, not in high-tonnage automotive green-sand lines [S3]. For very high tonnage or for sand landing at 165°C, the staged drum (flash cooling, pre-mix on conveyor, final drum cooling) remains the published reference design [S1].
Moisture, fines, and the dust problem
Evaporative cooling is a moisture-management exercise. The standard target after flash cooling is roughly 3% residual moisture by weight, which the next two stages evaporate to land the sand near ambient [S1]. Fluidized-bed systems meter water in for the same reason and rely on vibration to keep the bed from channelling, with hood geometry tuned to minimize dust entrainment [S2].
The cooler-muller approach sidesteps the dust-handling penalty by humidifying the sand before opening the air register, which keeps bentonite and coal dust in the mix instead of letting them ride the exhaust [S3]. That detail is the single biggest reason integrated units can sit inside a foundry without the baghouse that a continuous air cooler would require, and it is also why binder consumption drops when the cooler and muller are one machine [S3].
When a stand-alone cooler is still the right call
Three plant profiles should still buy a separate cooler. First, low sand-to-metal ratio systems (5:1 and below) where shakeout sand hits 165°C; the 40°C drum delta-T in the third stage is mandatory and there is no equivalent batch path [S1]. Second, high-tonnage continuous lines where the 100 cfm per tph air demand rules out cycle-time-bound cooling inside a muller [S1]. Third, plants that already run a chilled-water loop and want a finned-tube MD Cooler that ties into existing HVAC-class utility water rather than adding dust collectors and exhaust fans [S4].
Jobbing foundries running many pattern changes per shift with shifting sand-to-metal ratios are the canonical case for staged cooling, because the system rides out hot batches and cold batches without operator tuning [S1]. Continuous fluidized-bed coolers suit foundries that want three-stage cooling (controlled water addition, aggressive mixing, fluid bed) integrated into a return-sand belt with PLC-based temperature control on multiple bed points [S2].
Selection criteria in one comparison
On four decision criteria, the three architectures line up as follows. Footprint: integrated cooler-muller is the smallest, fluid bed and rotary drum both add a dedicated unit upstream of the muller [S3][S4]. Throughput ceiling: rotary drum and fluid bed handle 100 tph-class duties, integrated cooler-muller is bounded by muller pan capacity [S1][S2]. Dust and fines handling: integrated unit wins because the bed is humidified before aeration [S3]; fluid bed and rotary drum both rely on hood and baghouse design to control carryover [S2][S4]. Utility demand: MD Cooler wants chilled or tower water, air coolers want 100 cfm per tph of low-pressure air, and the integrated unit needs both but at smaller scale [S1][S4].
For plants specifying new equipment, the practical workflow is to measure shakeout temperature and sand-to-metal ratio first, then size the cooler from the 100 cfm per tph rule of thumb, and only then consider folding cooling into the sand mixer if the tonnage and temperature budget both fit inside one muller cycle. The role of the power mixer in the mulling step is unaffected when the cooler is stand-alone, but a cooler-muller can let the muller run a shorter cycle because cooling is co-located, which is part of where the throughput-per-machine gain comes from.
Trackable signals for follow-up: monitor shakeout temperature trends as sand-to-metal ratios drift, watch for new cooler-muller installations in iron and aluminum foundries as a proxy for adoption, and re-check baghouse loading when a continuous fluid bed replaces a drum, since dust entrainment is the most common downstream issue after a cooler swap [S2][S6].
See also our earlier report, BeCu vs CuCrZr plunger tips: wear, life, and beryllium health risk.