
V-Process Binder Cost: Savings, Tradeoffs, and Limits
V-process eliminates chemical sand-binder purchases, but film, vacuum equipment, energy, and labor remain, so total moldmaking cost is not eliminated.
Read →Industry News · Category
V-process eliminates chemical sand-binder purchases, but film, vacuum equipment, energy, and labor remain, so total moldmaking cost is not eliminated.
Read →
Tilt pouring reduces turbulence and inclusion severity versus static gravity pouring, but its defect benefit depends on mold design, filling control, and solidification.
Static pressure molding can reduce shop-floor noise, but the reduction depends on eliminating pressure-loss-driven impacts and controlling mechanical vibration.
Shell molding usually gives a smoother, more accurate casting than green sand, but tighter geometry does not guarantee fewer machining operations or defects.
Small foundries can gain from sand reclamation when avoided sand and disposal costs exceed equipment, labor, and testing costs.
Sand blasting and shot blasting produce different finishes: sand often yields a smoother profile, while metallic shot usually creates greater texture and coating adhesion.
Yes. Resin sand usually costs more per mold than green sand because binder material and slower cycles raise foundry cost.
Hydraulic shearing can leave a rougher, burrier edge than sawing, but a well-aligned shear can produce clean, smooth cuts with little post-cut finishing.
Hot-chamber machines generally use lower clamping tonnage than cold-chamber machines, but alloy, part size and geometry determine the required capacity.
Hot box core making consumes more process energy than cold box curing because it uses heated tooling, while cold box cures at room temperature.
An automatic molding line can pay back faster at high volumes when cycle time, labor, scrap, and tooling costs are modeled against realistic output.
Aluminum die casting does not require a different die material merely because the cast metal changes, but its higher temperature and abrasiveness demand a more wear-resistant tooling system.
Air-assisted sand filling improves fill uniformity over gravity dropping, but the benefit depends on airflow control, sand condition, flask geometry, and compaction.
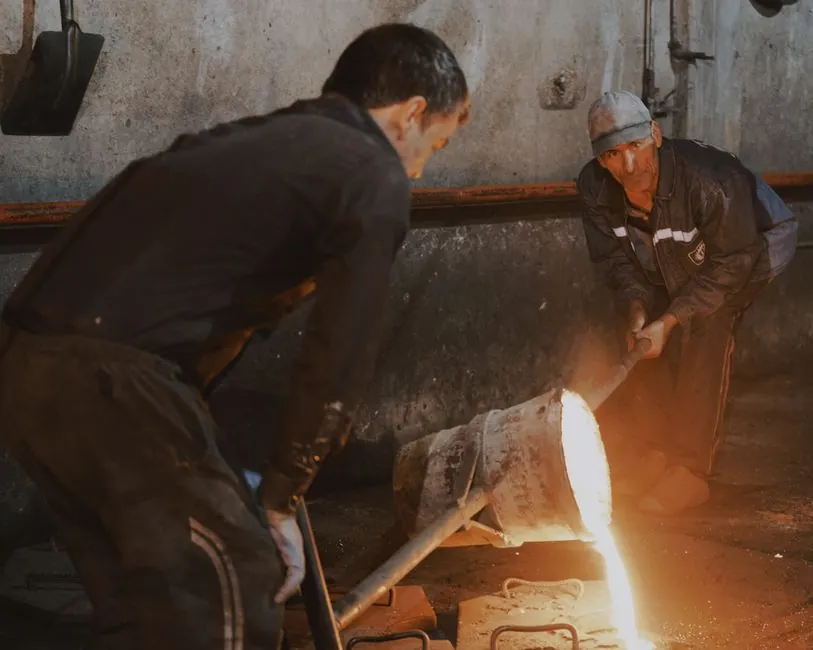
Shell core shooters usually need less curing time than hot box shooters because only a resin-bonded shell must harden, with published shell cycles of 40–120 s.
A shell core machine can produce stronger cores than a shooter-type machine because it combines resin-coated sand, heat curing, and controlled compaction.
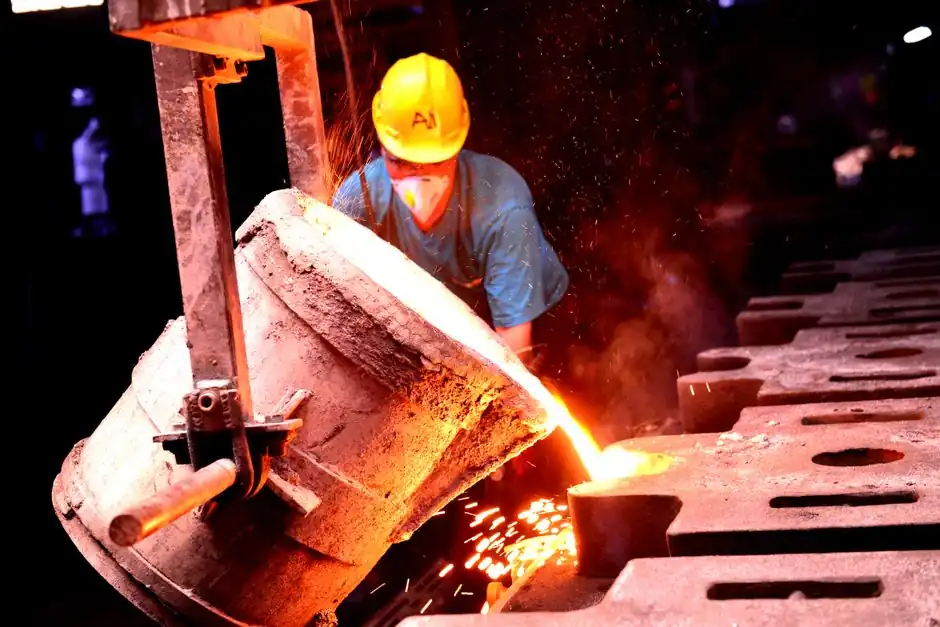
A custom mold base costs more than a catalog base when added machining, features, or nonstandard dimensions are required, but the premium varies by project scope.
Cold-box cores often evolve less gas than shell cores, but binder formulation, resin content, and casting temperature can reverse the result.
Bottom-pour ladles can reduce slag carryover by drawing steel from below the surface, but zero slag casting depends on correct stopper and ladle practice.
A divided blast cupola can raise iron melting rates from 3 to 6 t/h while reducing coke use, but it requires redesigned air distribution, controls, and refractory interfaces.
Choose direct squeeze casting for large, high-integrity parts; choose indirect for die-casting integration, automation, and complex cavities.

For hot-chamber zinc dies, water is the preferred TCU medium when die temperatures stay below 180°C; use oil above 200°C or when higher-temperature capability is required.
Choose a hardened-steel die-casting base for molten aluminum or zinc, and a configurable steel or aluminum injection base for lower-temperature polymers.
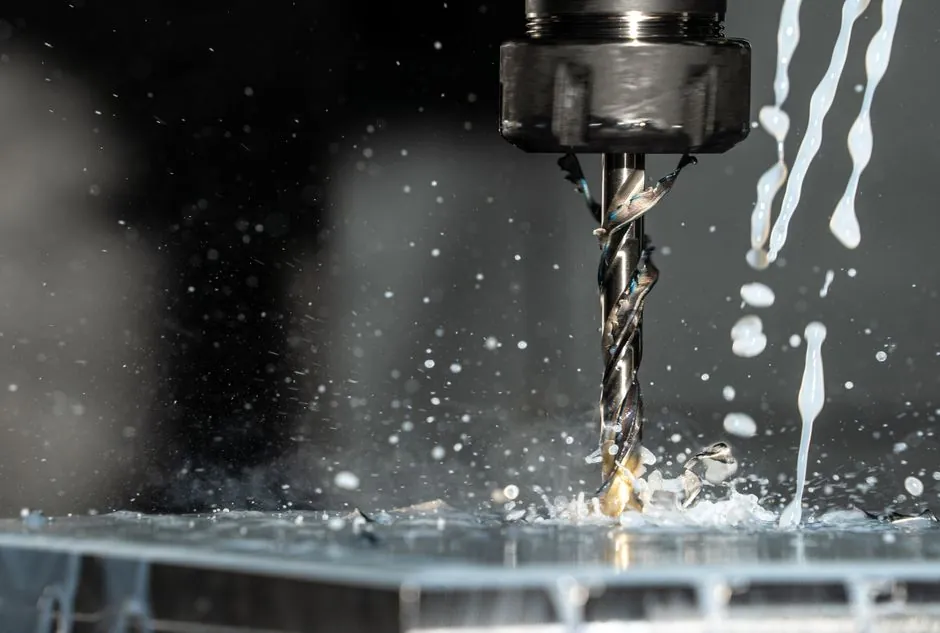
Die casting injects molten metal into a hardened steel die under high pressure, while injection molding uses heated thermoplastic material.
Die mounting clearance starts with the machine tie-bar opening, but platen size, die thickness, shot position, and service access determine whether the tool can be installed safely.
Select die casting capacity by projected area for clamp force and cold-shot weight for metal delivery; either constraint can govern the machine size.
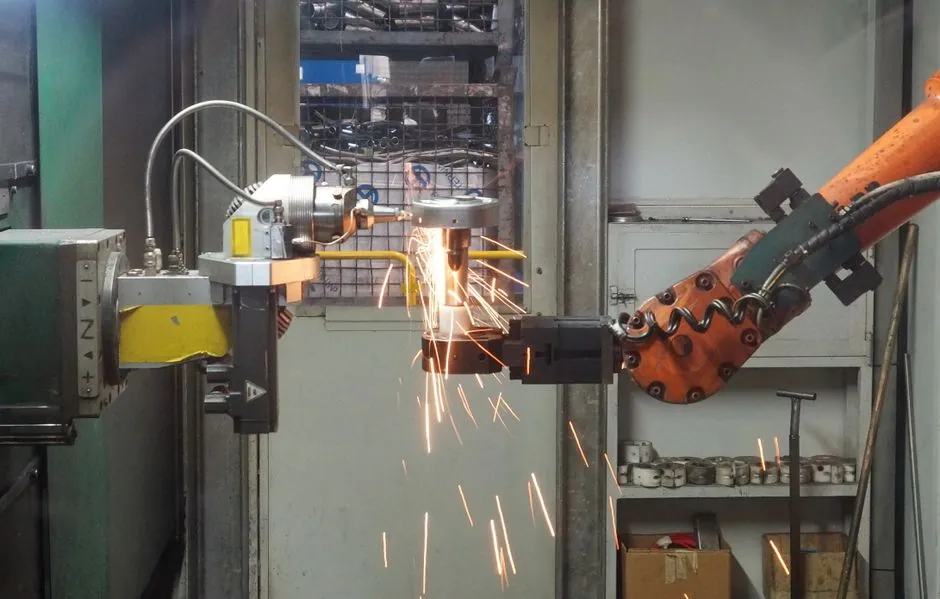
Select a cold-chamber aluminum machine for larger thin-wall electronics housings; use hot-chamber zinc only for compact, precise parts. Size by alloy, flow, shot, die and output.
Select a large cold-chamber HPDC machine sized by die area, shot weight, and 10–175 MPa injection demand, not tonnage alone.
Compare platen size with usable die dimensions, but require clamp force, tie-bar clearance, die height, stroke, and shot capacity to pass independently.
Platen parallelism tolerance controls die alignment, but no universal value applies. Set it from die deflection, parting-line fit, wear margin, part tolerance, and measured machine condition.
In a conventional cold-chamber die-casting machine, the pump charges the accumulator, holds the die closed and supports intensification, while the accumulator delivers the fast shot.
Intensification pressure is applied at the end of cavity filling to pack the metal as it solidifies, within a process that includes die filling, pressure intensification, and solidification.
Typical injection pressures for a hot-chamber die casting machine are between 1,000 and 5,000 psi.
Die-casting hydraulic-system pressure and flow-rate demands vary significantly throughout the cycle, and many older systems are greatly oversized.
A servo-pump die casting system can cut electrical energy use by 40–60% versus a fixed-speed hydraulic pump, with actual savings determined by cycle demand.
Select the ejector system by required stroke, pull force, die action, and shot size. Typical listed machines use 85–125 mm strokes and 108–180 kN forces.
Estimate die casting output from dry cycle time, then apply planned downtime and quality factors. A 4-second dry cycle yields 900 shots per hour before losses.
Die casting machine values depend on tonnage, age, hours, condition, and support: use 7–15 years as a broad manufacturing benchmark, then value each machine individually.
Choose a PLC with motion or hydraulic-servo modules for standard die-casting axes; use a dedicated motion controller for demanding multi-axis cycles.
Select die casting clamp tonnage from total projected area multiplied by cavity pressure, then apply a 20% to 40% margin and verify shot capacity, die space, and usable clamping force.
A new multi-cavity die-casting die typically requires 8–16 weeks for production tooling, while a complete launch program commonly takes 14–24 weeks.

For a mid-size aluminum part, budget roughly $5,000–$75,000 per die, with cavity count and geometry driving the per-cavity cost.

Single-cavity die casting tooling costs less upfront, while multi-cavity tooling lowers unit cost at volume but requires greater balancing and maintenance.
Zinc dies commonly reach 750,000–1,000,000 shots versus about 100,000 for comparable aluminum dies, but geometry and maintenance decide actual life.

Use a 0.5–1.0% linear die-casting allowance for aluminum, then validate it by alloy, geometry, thermal balance, and first-article measurements.
SKD61 steel cooling channels remain the practical die standard, while pure-copper liners improved test cooling by 12% but add bonding and integration complexity.

PVD is usually the stronger surface-engineering choice for molten-aluminum die wear, while nitriding is the lower-complexity base treatment; duplex treatment often performs best.

Replace a worn cavity insert when its geometry remains serviceable; replace the full die when the core, cooling, slides, or support structure has degraded.

A $50,000 die casting tool adds $5.00 per part at 10,000 units but only $0.50 at 100,000, making volume the key amortization variable.

Use an oxygen probe for continuous carbon-potential control in carburizing furnaces, then verify it with shims or dew point because probes can drift.

Dense-phase pneumatic conveying moves reclaimed foundry sand in low-velocity slugs, reducing wear and energy use compared with booster-assisted dilute systems.
Compare rotary argon degassing with vacuum degassing for aluminum: rotary is faster and lower-cost, while vacuum offers stronger gas removal at added cost.

Choose induction melting for clean charge control and alloy precision at foundry scale; choose the electric arc furnace for bulk steel duty where oxidizing refining and scrap tolerance dominate the tonnage math.

For small-batch aluminum foundries, tablets offer low-cost flexibility, while rotary inert-gas units deliver faster, more controllable hydrogen removal.
Plan 20–30 minutes for RH treatment and 30–70 minutes for ladle VD/VOD, then verify the cycle against ladle mass and steel grade.
Rotary aluminum degassing typically needs 5–15 minutes per holding-furnace batch, while 8–15 minutes covers batch treatment across varying melt volumes and starting hydrogen levels.
Aluminum degassing-box relining cost per cycle depends on refractory price, campaign life, metal penetration, repair frequency, and production loss.
RH degasser refractory life is best tracked in heats and erosion rate, with a common snorkel campaign of 550–600 heats. Aluminium degassing boxes can last 2–3 years with improved lining designs.
Degassing unit cost per ton depends on melt mass, rotor capacity, gas, consumables, installation, and energy, with no verified universal price range.
Argon generally removes hydrogen faster from molten aluminum, while nitrogen lowers operating cost but may require more gas, longer treatment, and tighter process control.
Use nitrogen at 99.99% purity for aluminum degassing, with moisture below 10 ppm and oxygen below 5 ppm, to improve hydrogen removal.
Onsite PSA nitrogen can reduce aluminum degassing gas cost to $0.01–$0.03/Nm³, versus $0.80–$1.50/m³ for purchased nitrogen.
Quality graphite rotors for aluminum degassing typically last 4 to 8 weeks under continuous operation, while shafts usually outlast rotors. Ceramic lacks comparable aluminum-foundry service-life data.
Choose degassing gas flow by melt volume, not melt mass. For aluminum, higher flow needs more rotor RPM to disperse the added gas into fine bubbles.
Rotary impeller degassing outperforms stationary gas-lance treatment for aluminum melts by producing finer bubbles, faster hydrogen removal, and uniform mixing.
Cupola furnaces suit continuous gray iron production above 40 t/h, while rotary furnaces favor flexible, smaller batches with stronger oxidation control.
A cupola-to-EAF conversion demands a plant-specific model covering electrodes, power, refractory, gas cleanup, iron chemistry and lost production.
A 10 t/h cupola requires about 1.22 m internal diameter at an 8.1:1 metal-to-coke ratio; typical shells span 450–2,000 mm and deliver 1–30 t/h.
Plan cupola relining around measured wear, iron and slag attack, and repair readiness, not a fixed calendar interval. A staged inspection and monolithic repair program can extend lining life.
Typical cupola metal-to-coke ratios span about 8:1 to 13.5:1, but furnace size, fuel quality, blast, and charge conditions determine the feasible target.
A small cold-blast cupola melts about 2–10 t/h, while a blast furnace runs continuously at steelmaking scale, making the cupola faster to start but not a pig iron substitute.
Choose cupola hearth depth from required melt rate, not furnace height alone: 1–30 t/h designs are available, with about 60% cold-blast efficiency.
A well-operated cupola commonly uses about 10–15% coke by metal-charge mass, equivalent to roughly 100–150 kg of coke per tonne of iron melted.
Calculate cupola charge-bed height from blast rate using furnace geometry, charge size, and coke-bed targets, then verify it against melting demand.
Cupola afterburners should verify CO destruction with continuous stack-gas analysis, not temperature alone. The research establishes hot-blast recuperation and combustion control, but gives no universal afterburner setpoint.
Crucible furnaces suit clean, batch nonferrous melting; rotary furnaces handle mixed, contaminated scrap but require stronger process control.
For production tool steel hardening, choose a controlled-atmosphere or vacuum furnace; reserve crucibles for melting and a resistance pit furnace for large vertical workpieces.
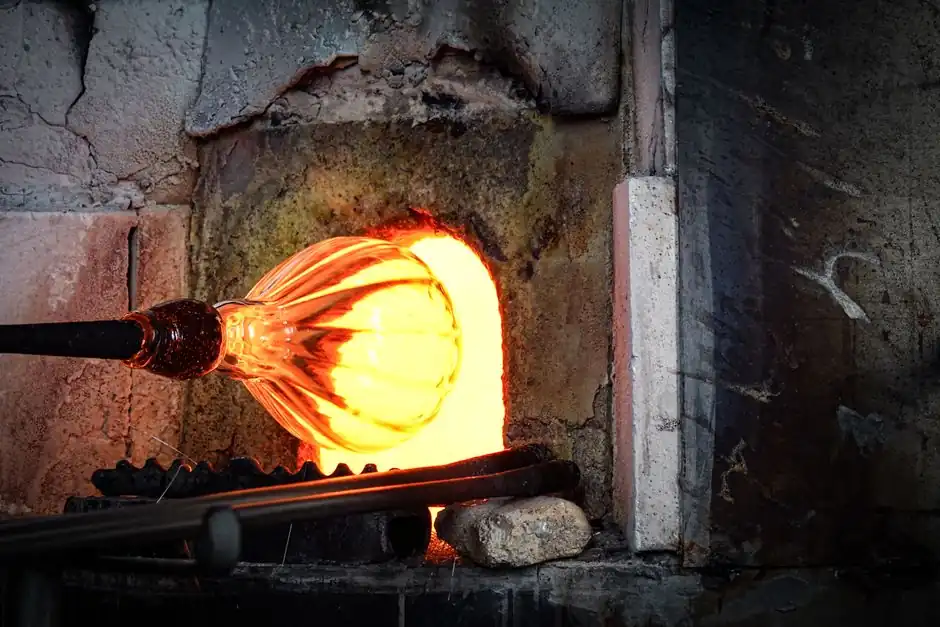
For small-batch bronze casting under a few hundred kilograms, a gas or oil-fired crucible furnace wins on capital cost, energy source flexibility, and alloy flexibility, while an induction furnace wins on melt speed, temperature control, and workshop cleanliness. Choose the crucible furnace when bat
Tilting and lift-out are the two main crucible-removal mechanisms in non-ferrous foundry furnaces. Pick tilting for batches above roughly 100 kg of aluminum or for ladle-fed HPDC/LPDC cells; pick lift-out only for sub-50 kg artisan or jewelry work where portability outweighs safety risk.
A stationary stand-crucible furnace suits small foundries and bale-out work under 1,000 kg, while a tilting mechanism is the right pick when a 1,500 kg pour, hydraulic safety, or clean ladle transfer is required. Decide by batch size, alloy changeover frequency, and operator distance from the pour s

Silicon carbide crucibles deliver thermal-shock resistance suitable for induction, gas, and resistance furnaces up to roughly 1,600-1,800°C, but require a staged preheat (200°C hold, ramp to 800-900°C) to avoid cracking from retained moisture. They outlast generic ceramic crucibles and tolerate rapi
Crucible furnace refractory lining life typically runs 80 to 400 melts per campaign in foundry service, with the spread driven by melt temperature, metal chemistry, electromagnetic stirring, and lining installation quality. Silica (quartzite) dry-vibration linings lead in grey and ductile iron, whil
Propane delivers roughly 46.4 MJ/kg lower heating value versus pipeline natural gas at about 50 MJ/kg, but its higher vapor pressure and ~10-15 PSI burner feed make it the default for portable crucible furnaces. Pipeline natural gas wins on per-BTU cost only when a utility main already exists at the
Crucible furnace capital cost per kg of melt capacity ranges from roughly $8/kg for 1 t gas-fired aluminum units down to $1.30/kg for hobby-scale electric kits, with mid-size 80–1000 kg non-ferrous units clustering around $10–60/kg driven by refractory, control package and heating method.
Crucible furnace power consumption splits sharply between active melt and standby: induction units draw 500-560 kWh/ton during a melt but only minimal holding power, while electric resistance crucible furnaces need continuous topping-up heat to keep metal at temperature. The right answer for a found
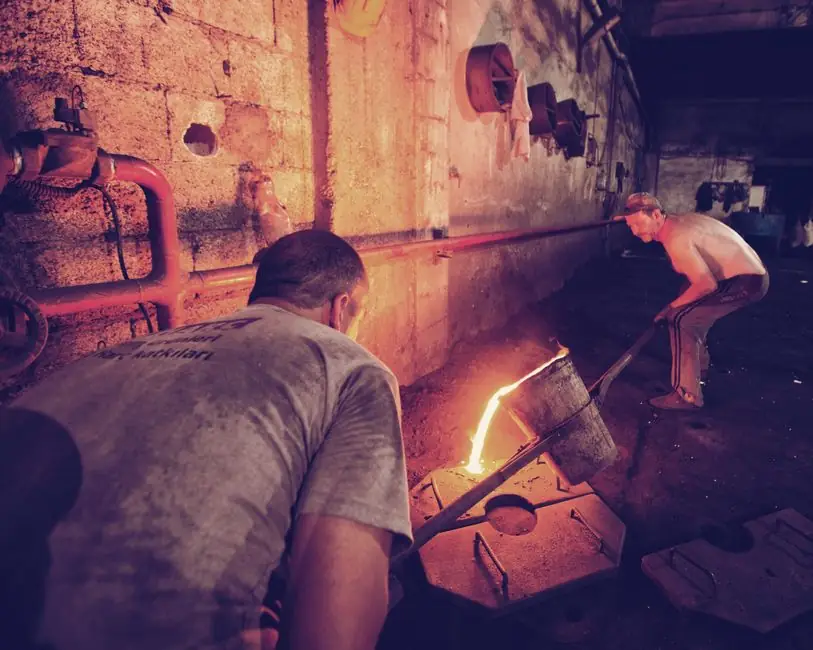
Natural-gas crucible furnaces consume 130–150 m³ of gas per tonne of aluminum melted to 720°C with cold-air burners, so fuel cost per kg of aluminum sits in the $0.04–$0.10 range at typical 2026 industrial gas tariffs. The dominant cost driver is burner type: recuperative units cut gas 25–38%, swing
Insulation thickness and material selection drive crucible furnace energy efficiency. Microporous boards at λ ≤ 0.14 W/(m·K) and 0.1–0.2 mm high-emissivity coatings cut heat loss, while DOE shows 10–25% savings from optimized insulation packages.
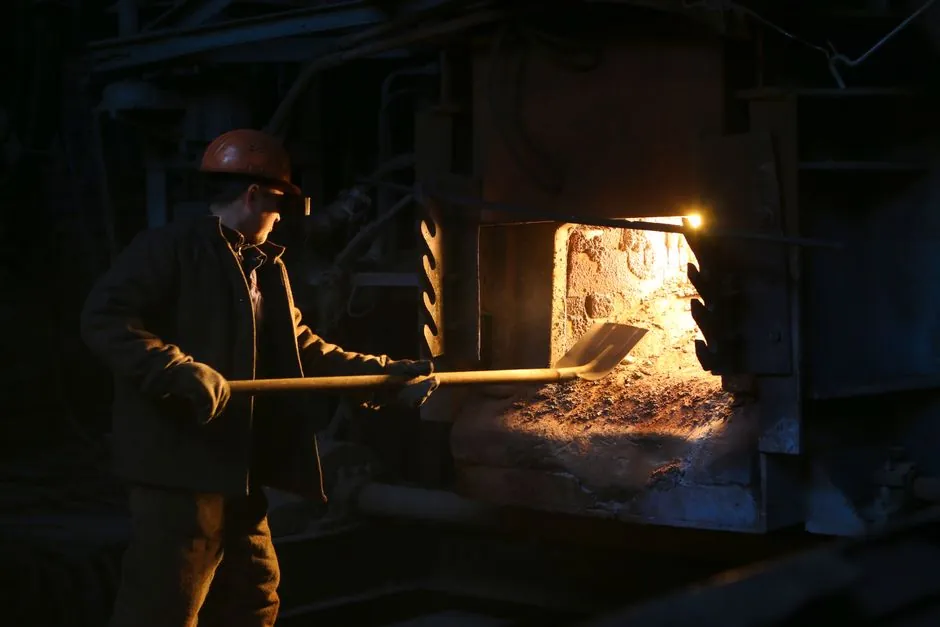
Crucible furnace melt rate per kilowatt scales with metal specific enthalpy and furnace efficiency: electric aluminum units reach 0.33–0.60 kg/h per kW of installed power, gas-fired brass melting typically lands near 0.59 kg/h per kW at 8.93% assumed efficiency, and induction iron melting consumes 5
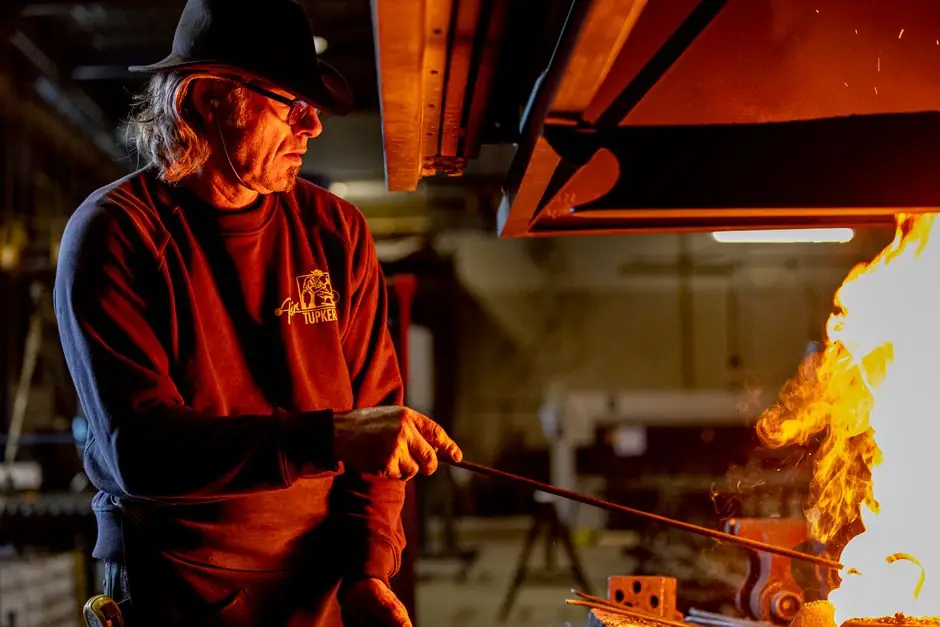
Crucible handling tongs and crucible pouring shanks serve distinct roles in foundry workflow: tongs lift hot crucibles from the furnace, while shanks hold and pour the melt at the mold. Selection hinges on crucible size (A6 to A20+), weight (8–30+ kg), operator count, and furnace loading style. Matc
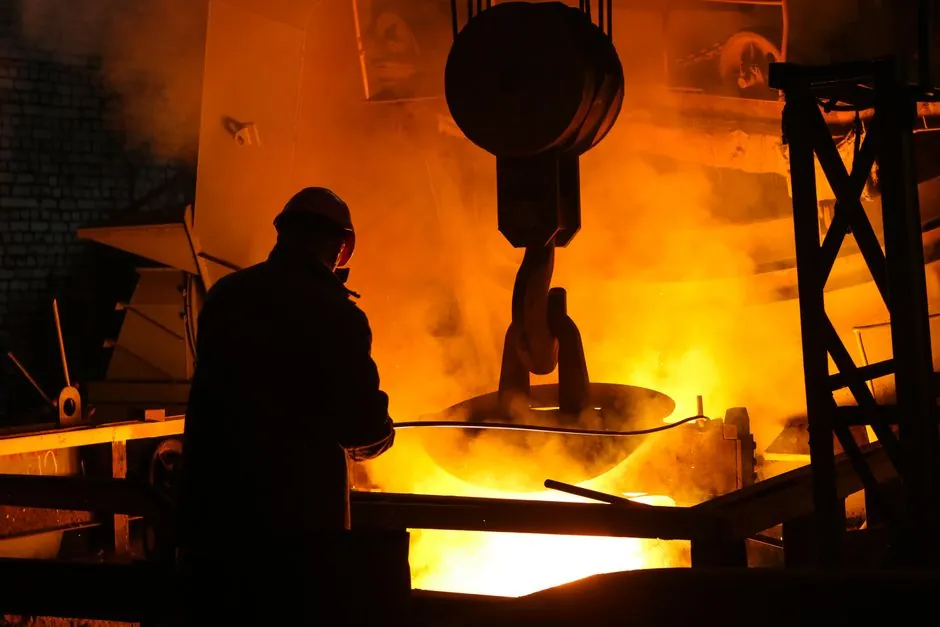
Clay-bonded and isostatic graphite crucibles deliver 80-150 melt cycles on aluminium, while a hobbyist-grade clay-graphite unit can fail in 20-30 pours. Pure graphite oxidises in air above ~400°C; clay-bonded grades trade graphite content (35-50%) for longer life. Spec by metal, temperature, and cyc
Gas-fired crucible furnaces deliver roughly 400 kg Al/h melt rate versus 250 kg Al/h for electric resistance units, but UC Berkeley testing shows electric melts yield mean tensile properties 20% higher with tighter distribution. Energy, melt loss, and alloy quality decide which technology fits.
Gas-fired crucible furnaces typically consume 130 to 150 m³ of natural gas per tonne of aluminum melted to 720 °C, with propane-fueled shop-scale furnaces burning around 7–8 kg/hr for a 25 kg brass-style charge. Per-cycle gas use scales linearly with charge mass, melt temperature and inverse efficie
Jewelry casting typically uses 50-500 g precious-metal charges in benchtop or dental-style crucibles filled to 85-90% capacity, while foundry casting uses 5-500+ kg ferrous or non-ferrous charges in industrial crucibles derated to 70-80% for high-temperature melts. Selecting the wrong size wastes en
Graphite is the default crucible for gold and silver melting under 1300°C, while zirconia, alumina, and noble-metal (Pt, Pd, Ir) crucibles are specified for platinum-group and reactive precious alloys above 1500°C, with the choice driven by chemical inertness, thermal shock, and melt temperature.
Graphite and silicon-carbide crucibles for foundry melting are commonly sized by rated melt capacity in kg, with model numbers from #16 (≈16 kg Al/Cu) up to 1500 kg for tiltable crucible furnaces and beyond 3000 kg for the largest aluminum crucibles. Working fill should stay at 80-90% of rated capac
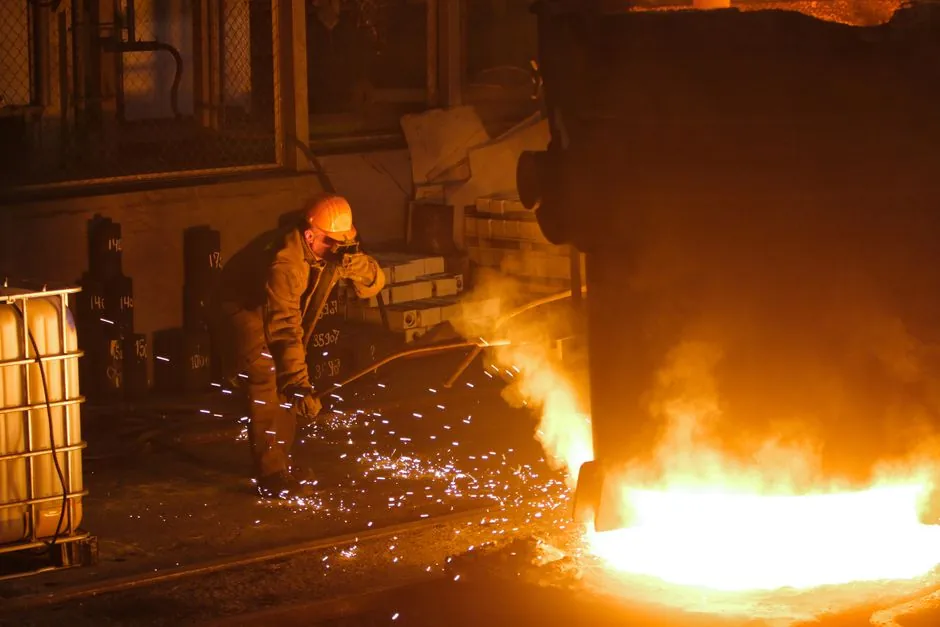
For a small foundry pour schedule, size the crucible furnace by usable molten metal per pour, not nominal capacity, then match heat source, tilt action, and heel practice to the alloy. Fixed furnaces cap near 1,000 kg Al, tilting units reach 1,500 kg Al, and electric melt rate sits around 250 kg Al/
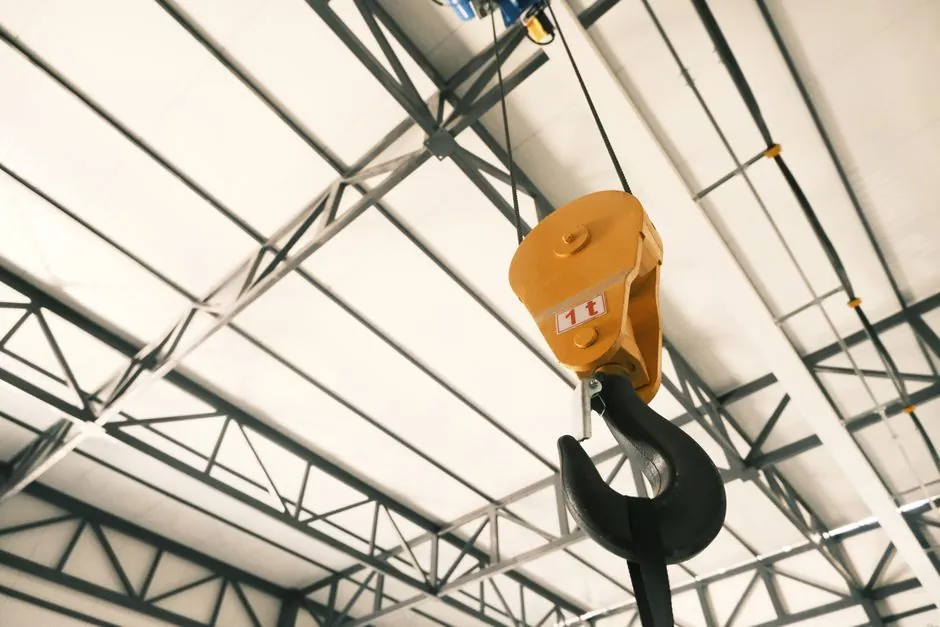
For loads under about 5 tonnes, crane loading onto a shakeout machine remains the lowest-capex choice; for 5–50 t flaskless or wide-flask molds running on a fixed cycle, automated mold transfer (AMT/AGV) wins on repeatability, floor-space, and dropped-load risk.
Bi-metal bandsaw blades typically run 2x to 6x the price of carbon steel stock and last 4x to 10x longer in mild steel, so cost per riser cut is usually dominated by abrasive wheels for steel pipe and by bi-metal for structural or abrasive alloys. Use this rule to pick the cheaper process per cut: a
Counter pressure casting (CPC) is a sealed-chamber evolution of low-pressure die casting that cuts gas porosity from 15% to 2% versus HPDC, at the cost of a larger pressure vessel and longer cycle. Specify CPC for heat-treatable, weldable, safety-critical aluminum parts; stick with standard LPDC or
Cold-box and hot-box core shooters differ fundamentally in curing energy: cold-box cures at room temperature via tertiary-amine gas catalysis, while hot-box cures against a 250–350°C die. Cold-box needs no heated tooling and uses 0.9–2% resin, offering fast cycles and complex thin-wall cores; hot-bo
Spiral paper core making machines cost Rs 3,00,000 to Rs 7,00,000 per piece in India (≈US$3,600 to US$8,400), with throughput from 750 to 2,000 kg/hr; cost per kg of core ranges from roughly Rs 1.5 to Rs 9.3, dominated by automation grade and capacity tier.
Core box clamping force in sand core making machines is set by hydraulic clamping, sized to hold the box still against shooting pressure (0.2–0.4 MPa blowing, much higher for core shooters) and gas-curing reaction loads. The right sizing rule is sand area × pressure, not machine maximum, applied thr
For a large automotive structural casting, select a cold chamber die casting machine rated 800–2400 tonnes locking force, with shot sleeve capacity 30–60% above the part's cold-shot weight, and verify alloy compatibility (Al/Si/Mg) against the die steel H13 thermal envelope.
Per-ton machine price runs 5-10x higher for cold chamber than hot chamber at equivalent locking force, driven by separate furnace, larger shot sleeve, and higher injection pressure hardware. Buyers should compare total cost per produced part, not sticker price, because cycle time and alloy selection
The casting ladle is the batch-transfer and ladle-treatment vessel that moves molten steel from the furnace to the caster top, while the tundish is the intermediate buffer/distributor sitting between ladle and mold that smooths flow, distributes to multi-strand casters, and bridges ladle swaps witho
Steel mill ladle cranes must lift ladle + liquid steel at the crane's rated capacity with a defined overload limit, typically 95%, and duty class A7–A8. Trunnion rings transmit that load through the ladle, so the crane SWL is the starting point for verifying ladle fit and the 25–50% structural safet
Ladle transfer cars suit short, fixed-route molten metal moves under 200 t, while overhead ladle cranes remain mandatory for full-capacity YZ class 75–400 t lifts and elevated pours above furnace or tundish level.
For 2026 ladle lining selection, alumina-magnesia-carbon (AMC) bricks outperform high-alumina bricks on thermal shock and slag-line life, with documented campaigns of 60 to 126 heats versus 20+ heats for first-grade high-alumina brick.
Steel ladles must be preheated to 800–1,100°C (1,472–2,012°F) interior surface temperature before receiving molten steel, with electric heating systems capable of 1,400–1,500°C (2,550–2,730°F) for high-tonnage operations and aluminum ladles held near 650°C (1,200°F).
Gravity die casting (GDC) fills a permanent steel mold under 2-10 minute cycles and 3-10 mm wall thickness, beating high pressure die casting on heat-treatable density but trailing it on thin-wall throughput. For a workshop upgrade, the decision turns on alloy (A356-T6 is the workhorse at 290 MPa te
An automated die-casting spray cell pairs a programmable sprayer robot with a release-agent system, an extract robot, and a die casting machine PLC link. Selection is driven by shot weight, cycle time, spray-zone count, and integration depth, with cold-chamber cells dominating aluminum work above 1
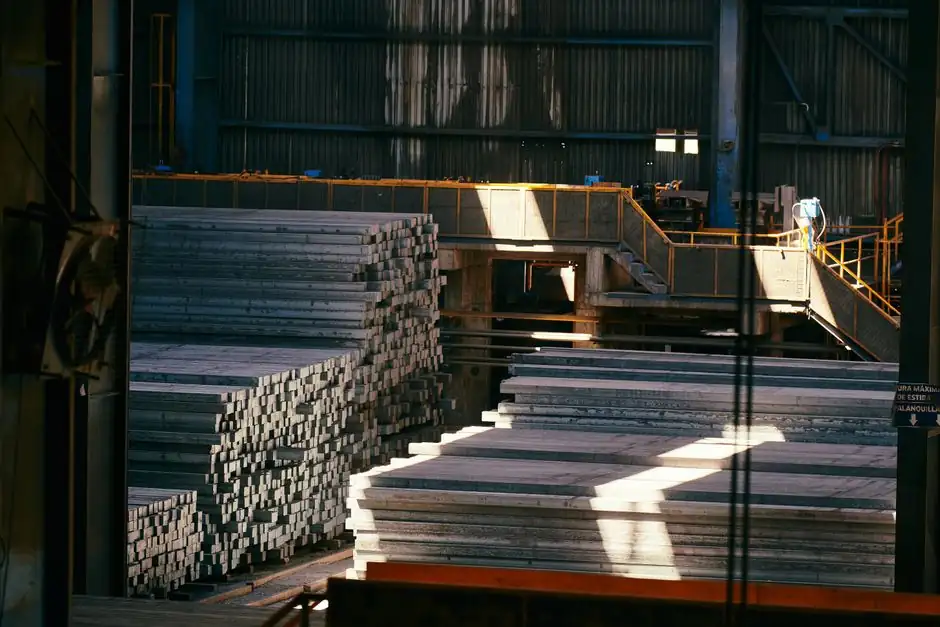
Continuous casting billet line selection starts with product mix, mould type, and strand layout, then locks in cooling and automation. Danieli curved billet casters cover 100–200 mm sections at radii 6–12 m, with up to 75 tph per strand on Fast Cast® and 2.4 Mt/yr at 12 strands. Match output target,
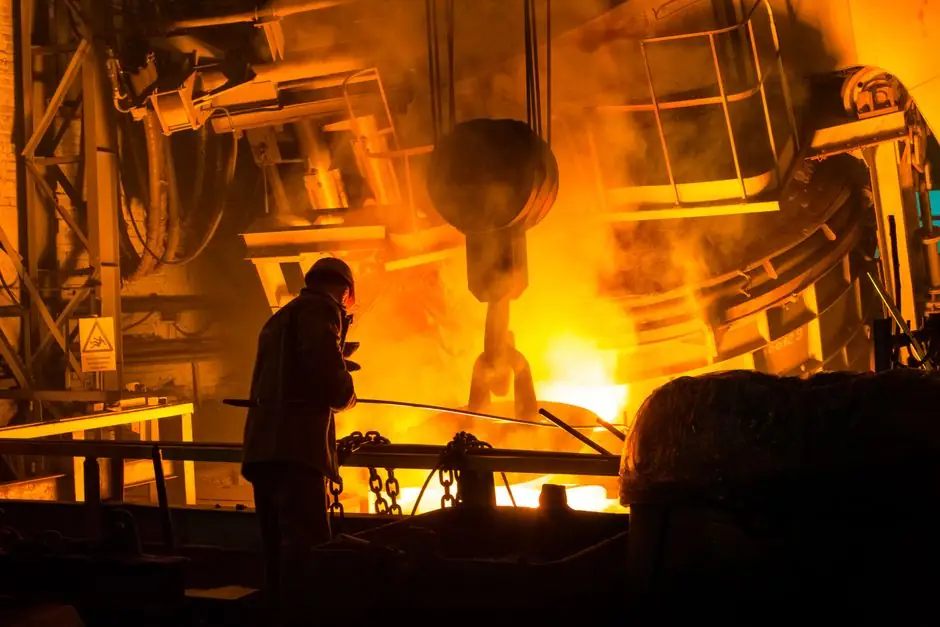
Centrifugal pipe casting requires a horizontal-axis machine set, a water-cooled metal die or sand-lined mould, a pre-heated pour spout, and a controlled pouring rate to sustain the 60–200 G rotational force field that defines the process. Selection pivots on pipe length-to-diameter ratio, alloy, thr
A small foundry startup typically budgets $98,500 to $780,000 for a complete mini-plant package, with individual molding lines starting at $30,000 and die casting machines from $50,000 used to $2 million new. Total landed cost rises another 20 to 30 percent once installation, training, dies, freight
Car bottom furnace hearth load capacity typically ranges from 1,000 to 5,000 kg/m² for standard builds, scaling up to 12,000 kg/m² on heavy-duty refractory cars for loads from 450 kg to 500 t. Subhearth castables rated to 1,315–1,425°C with 44–46% Al2O3 carry the practical design floor.
Coreless induction melting typically consumes 6-17 GJ per tonne of metal versus gas-fired crucible furnaces at similar duties, with the gap widening on cold-charge melts. Selection comes down to alloy, batch size, utility mix, and emissions ceiling rather than a single efficiency number.
Modern cold box cores using phenolic urethane PU binder routinely match or exceed the immediate (cold) strength of hot box cores while delivering higher dimensional accuracy and no heat cure. The trade-off is lower hot strength and higher binder cost, so hot box retains a niche where hot strength an
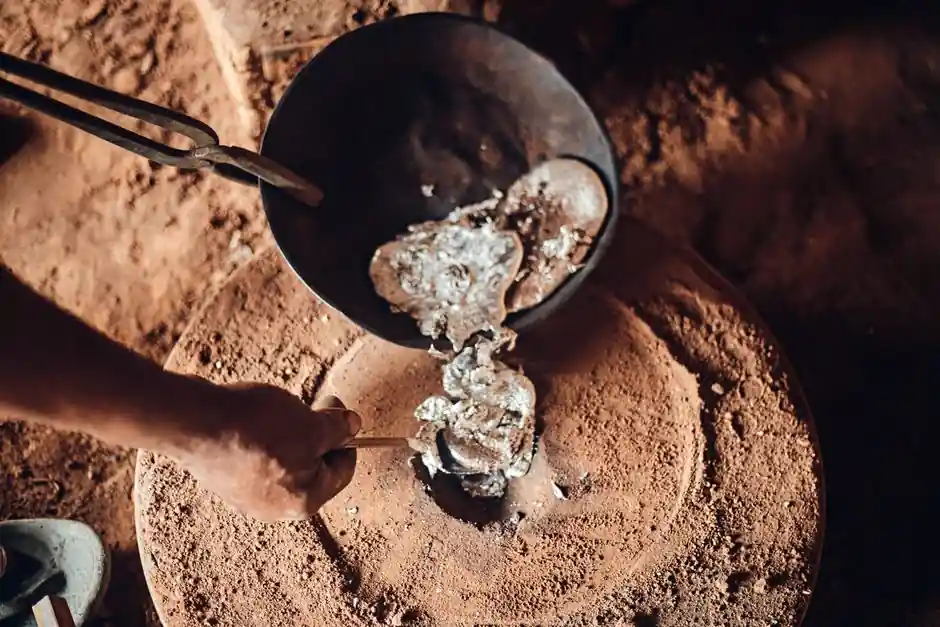
Clay-graphite crucibles remain the cost-effective default for non-ferrous melting below 1200°C, with SiC-graphite variants extending service life 2-4x in aluminum and zinc service. Selection hinges on metal, temperature, and flux exposure rather than raw material alone.
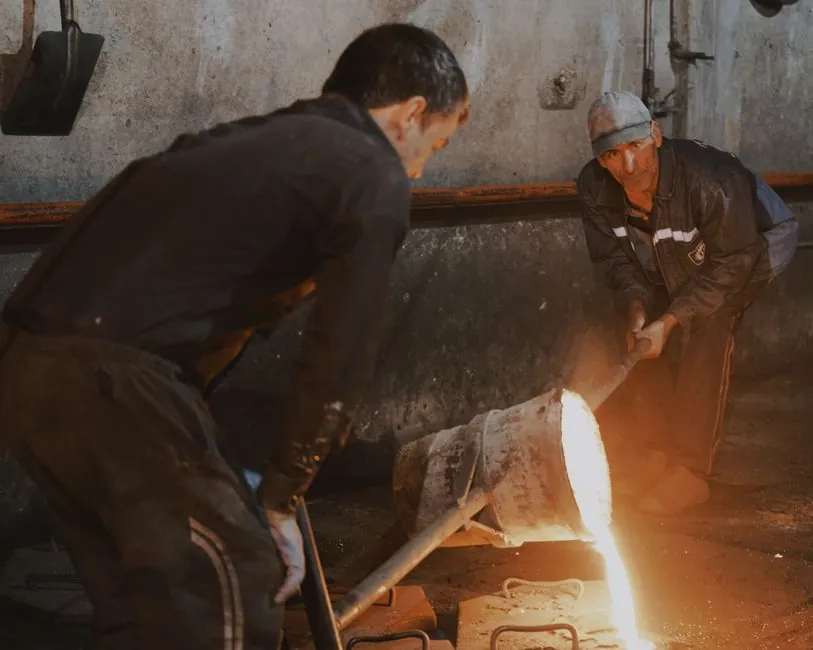
Sand-cored die casting tooling runs $5,000–$100,000+ for the die itself, while a matched shell core shooter tool adds $3,000–$15,000 per cavity box. Sand casting patterns stay at $500–$5,000, with the real break-even between 500 and 2,000 parts.
Cooling conveyors ahead of shakeout on high-volume lines must deliver controlled retention time so castings reach a safe, uniform temperature before shakeout machine entry, while limiting sand carryover into downstream cleaning.
Preformed inserts cut ladle change-out to under 30 minutes and give up to 50 fills on small steel ladles, while monolithic castables suit large shells (40 t plus) where thickness and thermal mass dominate. Pick the lining family by ladle capacity, pour type, and preheat discipline, not by habit.
Cast iron pattern plates deliver the longest service life and lowest per-casting cost in high-volume shell molding, steel wins on stiffness for tight-tolerance cores, and aluminum patterns are typically specified only for prototype or short-run work below ~10,000 cycles. Decision should follow produ
For zinc melting at 420°C, a cast iron pot is the standard low-cost choice for batches under roughly 50 kg, while a clay-graphite crucible becomes worthwhile once thermal cycling, purity, or higher melt rates matter. Selection hinges on three numbers: zinc's 420°C melting point, the cast iron pot's
Cartridge heater watt density for hot box core boxes typically falls in the 30 to 60 W/in² band for medium-duty iron foundry work, with high-watt-density units above 65 W/in² reserved for short heated lengths under 8 inches and tightly reamed bores. Specification must combine sheath material, fit to
Tungsten carbide-tipped (TCT) circular saw blades outperform HSS blades for aluminum gate cutting on speed, edge quality, and blade life, while HSS remains a budget option for thin, low-volume work. Use TCT with triple-chip-grind geometry at 60-100 teeth for 10-inch blades on plate, extrusions, and
Soda blasting can replace traditional silica sand blasting for paint removal on sheetmetal, fiberglass, wood, and thin-gauge substrates, but it does not remove rust or thick mill scale. Sodium bicarbonate (NaHCO3) media strips coatings without etching the substrate, at typical rental kit cost of $10
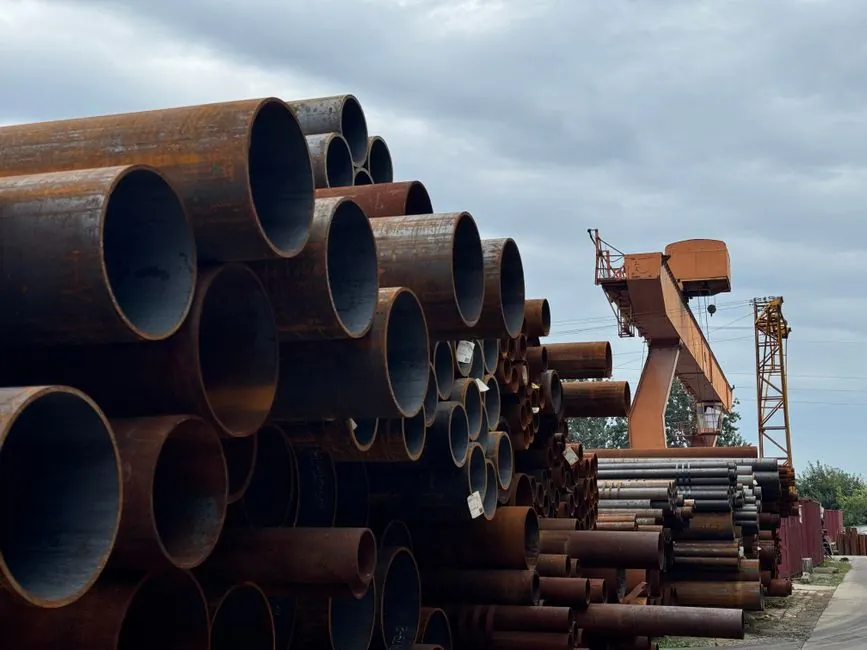
Shot blasting can fully replace acid pickling for oxide-scale removal on bars and wire rod in most carbon-steel applications, provided a pre-breaking step handles the brittle scale layer. Mechanically broken scale plus abrasive cleaning matches pickling on surface cleanliness while eliminating acid
Hot-box shell cores can serve as the thin bridge or inter-bore insert inside a water-jacket core, but the main bulk of a water jacket must be made as a separate, thicker cold-box or stack-moulded core. Mixing the two processes is established practice in crankcase foundries because the hot-box shell
Gravity die casting cannot match the wall-thickness floor of high-pressure die casting. Practical minimums sit at 3 mm for gravity versus 1.0–1.5 mm for HPDC, and the gap widens at thinner sections due to fill dynamics, not machine choice alone.
Yes. A 100–350 kg hydraulic-tilting coreless induction furnace is the realistic floor for a small jobbing foundry, with compact manual-tilting units going down to 10–100 kg for trial work. Below ~25 kW of input power, melt quantities of 2–5 kg of steel become marginal and the duty cycle dominates th
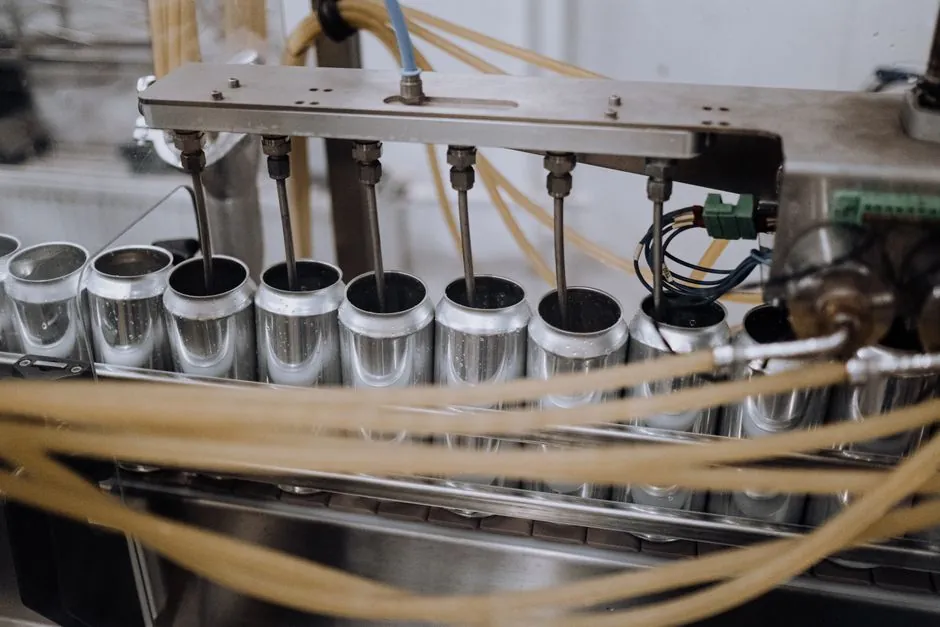
A zinc die casting machine can run multi-cavity dies at full tonnage when projected area times metal pressure (10,000 to 12,000 PSI) stays within the press rating; otherwise tonnage, not cavity count, gates feasibility.
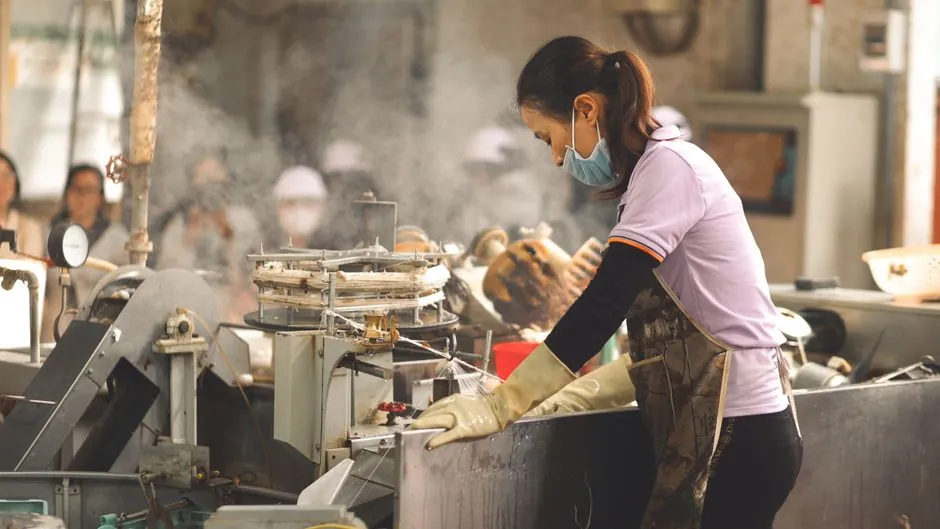
A shell core shooter and a hot box core shooter cannot make identical cores because they cure resin-coated sand at different temperature ranges and produce different wall geometries. Choose a hot box for solid, dimensionally accurate cores; choose a shell machine for thin-walled, hollow shells.
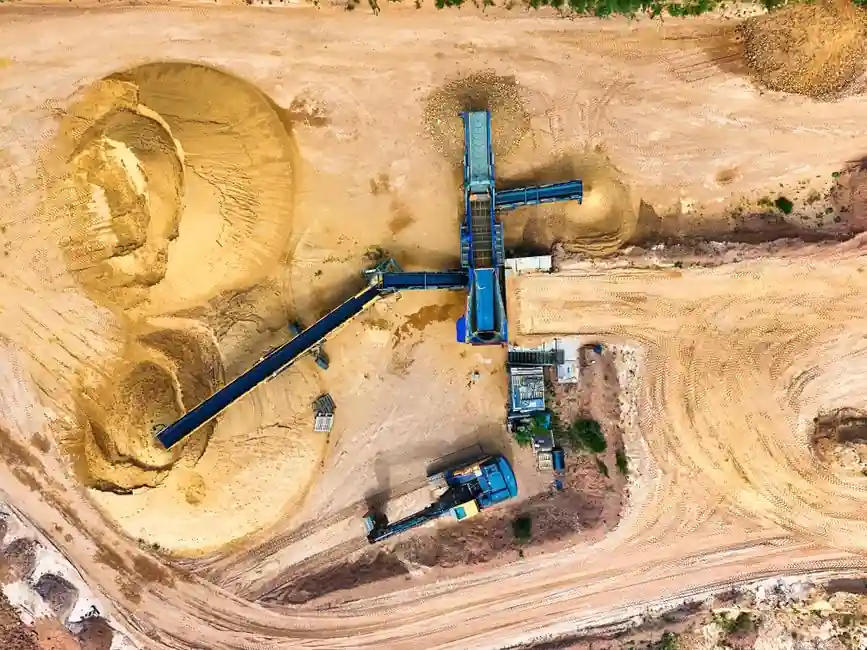
A combined cooler-mixer can replace a stand-alone sand cooler for green return sand in many batch foundries, but only when shakeout temperature, sand-to-metal ratio, and moisture-addition control all line up. Continuous high-throughput lines (e.g. 100 tph) and low-ratio systems hitting 165°C at shak
Bubble cap distributors hold pressure under hot fluidizing conditions and tolerate uneven feed, while 45° slotted nozzle plates cut minimum fluidization velocity and improve lateral mixing. For green-sand and resin-sand coolers handling coarse, abrasive hot return sand, cap plates generally win on d
A 1 cu ft blast pot holds roughly 50 lb of abrasive and runs about 15 minutes per fill, while a 6 cu ft pot holds around 600 lb and runs 60-90 minutes, so the right pick hinges on CFM, hose layout, and refill tolerance, not just vessel volume. Match the compressor first, then size the pot to the pro
Blast hose pressure loss scales linearly with length and roughly with the inverse fifth power of inner diameter, so 50 m of 10 mm ID drops ~7.5 PSI at 9.4 cfm while a 19 mm ID hose with a #6 nozzle can lose 11 PSI. Spec the hose ID equal to or one size above the nozzle orifice, and step up to 32 or
For die casting machine shot ends, piston accumulators handle higher pressures (exceeding 350 bar) and longer cycles, while bladder accumulators deliver faster response and lower cost on a 4:1 compression limit.
Beryllium copper (C17200, 1.8–2.0% Be) plunger tips reach HRC 38–42 hardness and 8–12% cycle-time gains, but machining them down for re-use exposes operators to beryllium oxide dust classified GHS Carcinogenicity 1. CuCrZr (UNS C18150) delivers 320–350 W/m·K thermal conductivity with zero Be, the pr
Batch shakeout fits no-bake lines running 20 to 30 molds per hour, while continuous shakeout matches automated green sand at up to 500 molds per hour. Match the shakeout duty cycle to the molding line's throughput and the sand binder's reclamation needs.
For aluminum riser and gate cutting on horizontal band saws, the working TPI window is 3 to 10 for solid stock above 1 inch and 10 to 14 for general 1/4 to 2 inch sections, with 6/10 variable-pitch bimetal blades (M42, 1/2" wide) the default production-floor choice.
An automatic turntable blast cabinet with fixed nozzles pairs a rotating work table with stationary blast guns, typically sized from 12 to 72 inches diameter with load ratings of 500 to 2,000 lb and 0-29 RPM drive ranges. Fixed nozzle geometry gives repeatable coverage, while the PLC-controlled turn
Automatic molding lines run faster but lose accuracy on complex internal passageways, while lost foam casting lines sacrifice cycle speed for ±0.005 mm/mm tolerances and 20-50% lower per-part cost. The right pick depends on whether the priority is throughput or near-net-shape complexity.
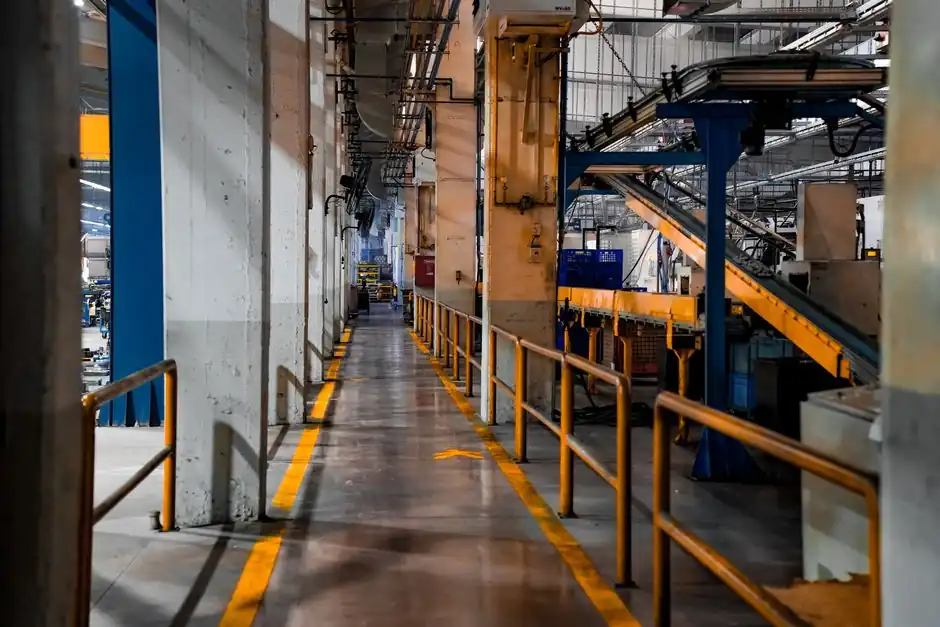
Automatic molding line total cost of ownership runs 2.5–5× the quoted per-part price once labor, energy, and quality costs are counted, while converting manual operations can cut direct labor by 50–80% per shift. Real payback lands in 2–4 years for mid-volume programs.
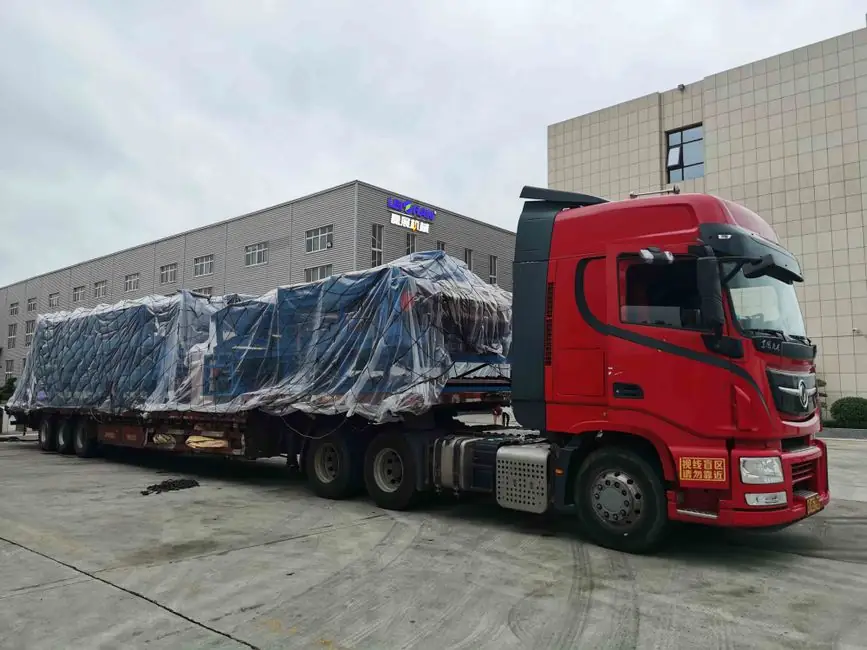
On an automatic injection molding line, amortized tooling typically runs $0.06–0.30 per part at 50,000 parts, while machine-hour cost dominates at $11–$85/hr across cavity counts that yield 164–2,618 parts/hr.
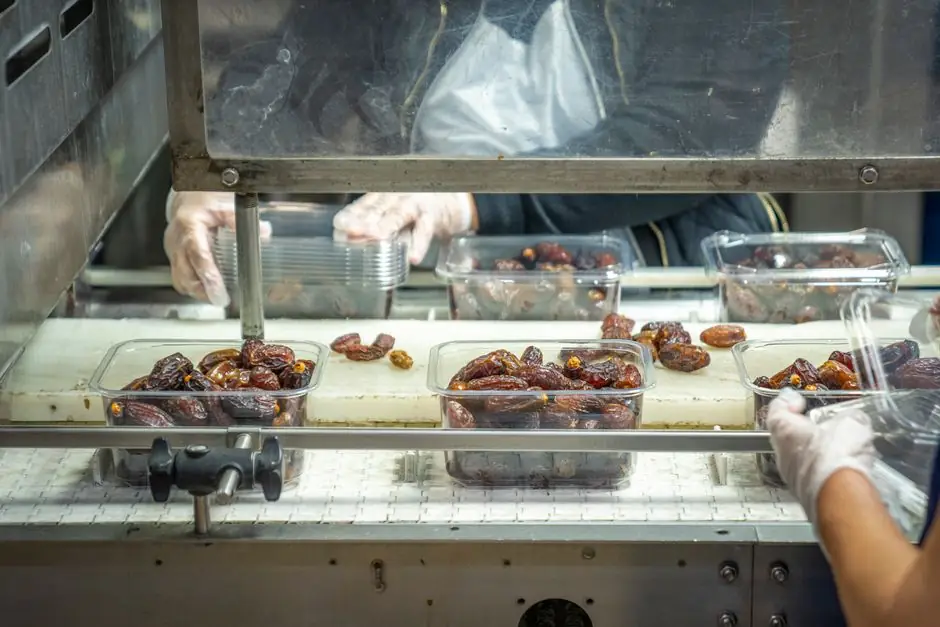
High-volume plastic injection molding output is set by the formula Cavities × Shots/hour, and a 16-cavity mold at a 22-second cycle reaches 2,618 parts per hour. Foundry automatic molding lines run 250 molds per hour, while maintenance on high-volume tooling can absorb 30-40% of capacity. Numbers be
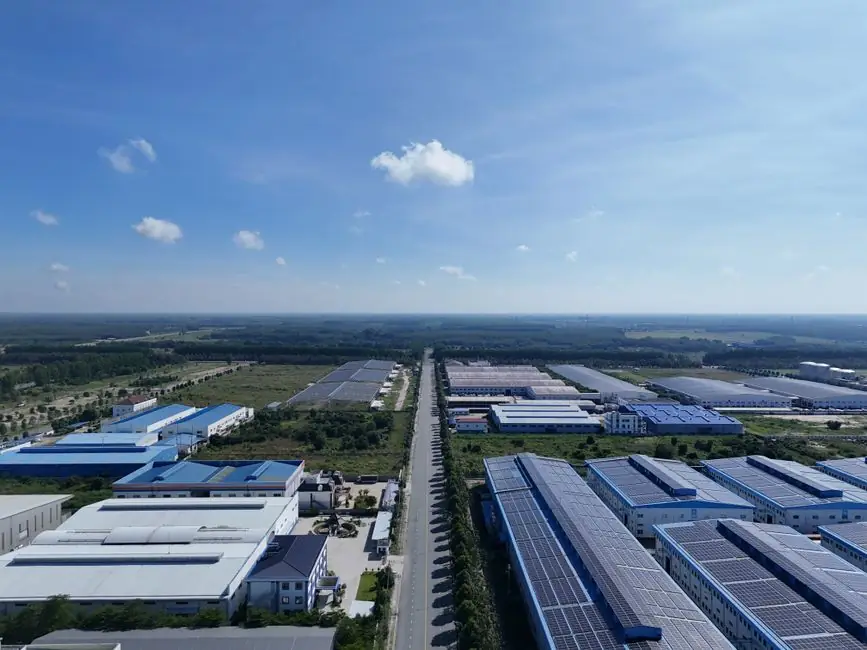
Hydraulic squeeze pressure on automatic molding lines is set per recipe through the operator HMI, with flaskless lines like the FDNX running on 80+ psi shop air and jolt-squeeze machines delivering sand mold hardness above HB90, while rubber/composite presses apply proportional valve-controlled hydr
Automatic molding lines in green sand foundries routinely exceed 400 molds per hour with no manual intervention, while hand-operated jolt-squeeze matchplate lines cap out around 60-120 molds per hour per operator. Injection molding cycle data shows 25% faster cycles add $50K-$150K annual capacity pe
Pattern-set changeover on an automatic molding line typically runs 30-90 minutes per swap on conventional setups, but SMED-based programs now drive that window below 10 minutes of true stop-the-clock time. Foundries that standardize pattern presets, add quick-clamp hardware, and split internal from
An automatic pattern change system executes the pattern swap inside the molding machine's own cycle, eliminating dedicated pattern-change downtime and lifting net molds-per-hour on a flaskless line. Operators stage the next pattern in an auto-changer magazine while the current mold runs, and the swa
Automatic molding lines equipped with core-setting robots routinely achieve 9-second core set times inside the cycle, and pairing the robot with servo-driven take-out and motion-controlled dry-cycle trimming can cut total cycle time by 12% to 55%.
On cold chamber die casting machines, the ladle volume and the machine's rated shot weight must be matched within a tight tolerance; robotic ladling holds shot-to-shot repeatability at 99%+, and an electric auto-ladle on the machine bus (TOSCAST) auto-compensates the biscuit when spray time changes.
Austempered Ductile Iron (ADI) is made by quenching austenitised ductile iron (850–900 °C austenitise, 20–40 min soak) into a 280–400 °C molten nitrite–nitrate salt bath; an integral quench furnace cannot match the salt's 600–1200 W/m²·K heat transfer coefficient or ±5 °C isothermal stability, so sa
Die casting typically beats sand and investment casting economically at annual volumes above roughly 20,000 parts, where high steel-die tooling cost amortizes across enough pieces. Sand casting dominates below ~1,000 per month; investment casting owns the low-to-medium band.
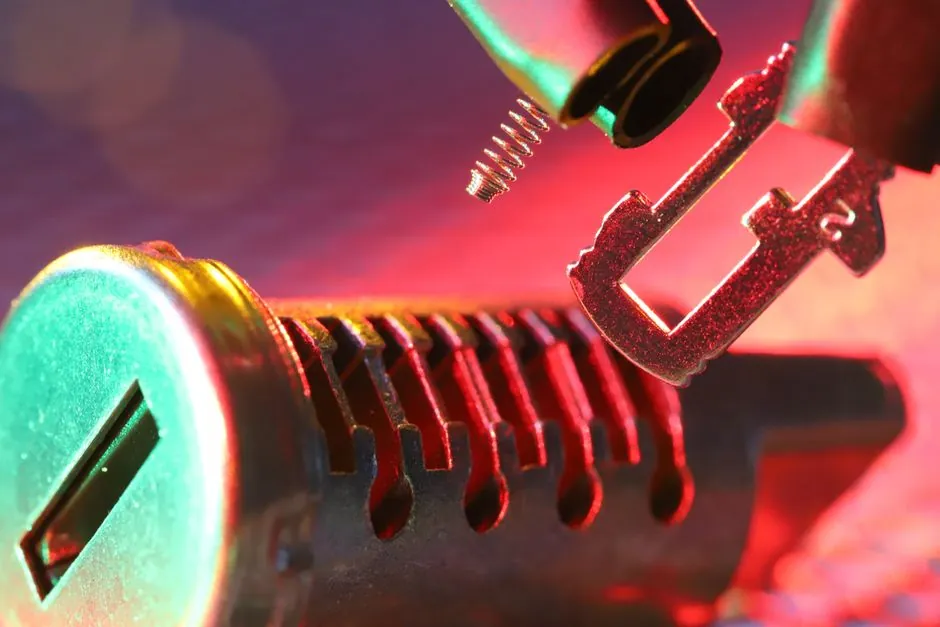
For die casting dies, choose angle pin slides for short-stroke, low-force undercuts on simple castings to minimize tooling cost; specify hydraulic core pulls when slide travel exceeds what the press opening stroke can deliver, when slide mass is high, or when multiple slides and complex cooling chan
Ammonium chloride (NH4Cl) is the dominant latent acid catalyst in hot box core systems; ammonium nitrate (NH4NO3) acts as an oxidizer, not a functional substitute, and chloride contamination of AN reduces its thermal stability. Foundries choosing NH4Cl get faster, lower-temperature cure; plants hand
PU cold-box amine and binder together cost roughly USD 0.9–2.0 per kg of finished core, driven by 0.4–1.2% resin addition and 0.05–0.15% tertiary-amine catalyst. The dominant cost lever is binder addition rate, not amine unit price, because resin is typically 15–25x more expensive per kg than amine
AM60B and AM50A both target crash-relevant magnesium castings, but their published elongation differs by roughly 1–2 percentage points (8% vs 9%) on 2 mm die-cast tensile specimens, and that small delta is the entire reason a designer chooses one over the other.
Aluminum ingot pass-through clauses in die casting contracts tie part price to the LME index, typically using a base alloy price plus a fixed conversion adder. With US Section 232 aluminum tariffs at 50% since June 2025, procurement must specify index, base date, scrap-recovery band, and tariff trea
Aluminum die casting cost per kg breaks down into four cost drivers that move the line item: A380 ingot ($2.80/kg), processing/machine time, labor and overhead, and amortized H13 tooling. A baseline simple 1 kg part runs $5.38 (material + machine + labor), while market quotes commonly land at $20–$3
Tie-bar strain gauging on aluminum die casting machines verifies true clamping tonnage by reading microstrain on each bar. Bonded foil gauges, magnetic clamp-on units, ultrasonic acoustoelastic probes, and digital tonnage encoders each carry distinct trade-offs in accuracy, install effort, and proce
Hold the shot sleeve fill ratio between 50% and 75% on cold-chamber aluminum die casting, target 60% for the cleanest slow-shot phase, and pair it with intensification pressure of 27-40 MPa to suppress gas and shrinkage porosity. NADCA-derived guidance, PQ²-style slow-shot velocity around 0.5 m/s, a
For an EV battery enclosure, a 2,500–5,000 ton cold-chamber HPDC running AlSi10Mg (vacuum-assist below 50 mbar) at 4,000–9,000 kN clamping force delivers single-piece battery trays with porosity under 0.1% and IP67 sealing.
For thin-wall electronics enclosures in 2026, cold-chamber HPDC on a 160-400 ton machine with ADC12 or A380 alloy is the default spec, targeting 1.0-2.5 mm walls and 60-180 s cycles.
Spec an aluminum die casting machine for a structural chassis part around cold-chamber HPDC in the 800–1,600 t clamping range, with A380 or AlSi10MnMg alloy, 1,500–25,000 psi injection, and a shot weight that leaves 30–40% pad margin on the machine's rated capacity.
Select a cold-chamber aluminum die casting machine in the 180-800 ton clamp range for motor housings, with 250-950 ton being the workhorse band for most EV and industrial motor programs. Match tonnage to projected area, pick A380 or AlSi10Mg alloys for thermal management, and require vacuum assist p
For a large aluminum gearbox casing, select a cold-chamber high-pressure die casting machine sized by projected area (clamp force), total shot weight, die envelope, and injection performance, typically in the 800-1600 t range with verified H7 bearing-bore machining. Cross-check alloy (A380, A383/ADC
Aluminum alloys A380, A356, ADC12, and A383 dominate die-cast heat sink production, with 0.5 mm thin fins and 50 mm fin heights achievable on cold-chamber machines. Selection of clamping force, plunger speed, and die temperature, not alloy alone, determines thin-fin yield for LED and power-electroni
Aluminum die casting machines carry higher tonnage and tooling cost (often 100-4,500 ton range) versus zinc hot-chamber machines (12-850 ton, $15,000-$250,000). Aluminum wins on per-part cost at volume; zinc wins on detail, tool life, and lower startup.
Plunger tip material choice drives aluminum HPDC uptime: beryllium-free copper-titanium and proprietary dispersion-hardened copper grades (e.g. AMPCO/AMPCOLOY) deliver the longest tip life, while nitride H13 hot-work tool steel and forged Con-Duct steel serve as lower-cost consumable options for sle
A356 aluminum melt in die casting is typically held 50-70°C above its liquidus, with a working melt range near 615-680°C and a die mold window of 200-280°C. Controlling these three temperatures separately is the single largest lever for reducing porosity, cold shuts, and premature die wear.
Aluminum die casting machine hydraulic systems are sized for fast shot speed by combining accumulator volume, intensifier cylinder area, and servo valve response to hold intensification pressures of 80–120 MPa with stable fill velocity. For thin-wall structural parts above 4 m, the bottleneck shifts
Servo-hydraulic aluminum die casting machines typically consume 0.8–1.2 kWh per kg of cast metal, with energy representing roughly 25% of total die-cast product cost. Retrofit and predictive-maintenance strategies can reduce that energy and repair spend by around 30%.
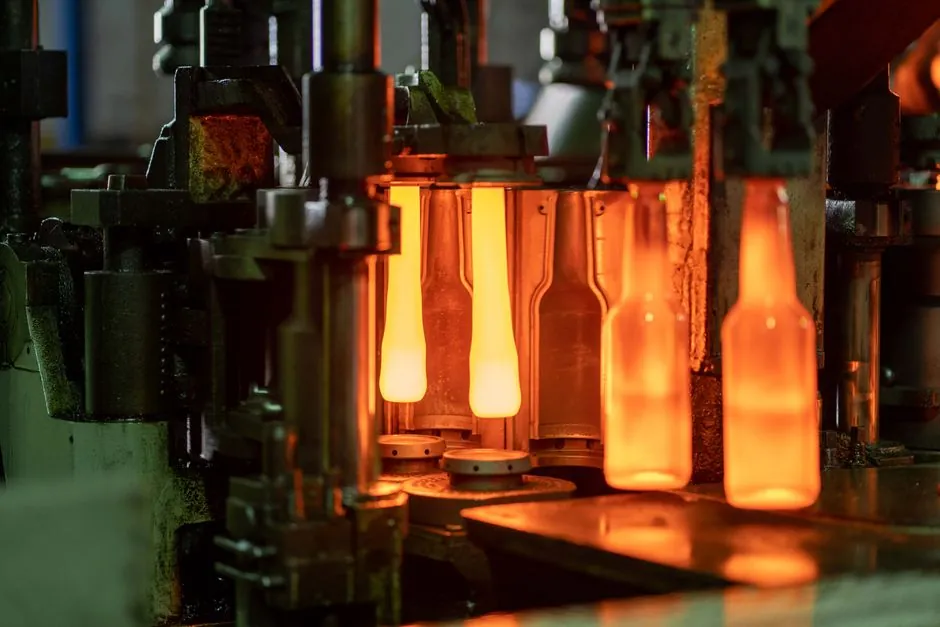
Die surface temperature swings from above 1000F (538C) at fill to under 500F (260C) after spray, so aluminum die casting dimensional stability depends on holding mold surface within roughly 200-280C and a tight control band, with A380 shrinkage of about 6.7% by volume setting the practical limit. Sp
H-13 die steel at HRC 42-50 remains the baseline for aluminum die casting dies, with thermal fatigue resistance improving as austenitizing rises from 1750 to 2050°F. Alloy 718 and premium maraging grades extend die life when die surface temperature exceeds 800°F (427°C).
Aluminum die casting dies typically deliver 75,000–200,000 shots before end of life, with 100,000 cycles commonly cited at 1060–1220°F melt temperatures using H13 or DIN 1.2367 tool steel. Real-world die life is governed by thermal fatigue, soldering, and erosion rather than raw shot count, so condi
Die coatings for aluminum die casting machines reduce soldering by creating a wear-resistant barrier between molten aluminum and tool steel, with PVD systems like Duplex-TIGRAL and CrN widely specified for high-volume HPDC cells. Soldering, washout and heat checking remain the dominant failure modes
For thin-wall automotive aluminum housings, a cold-chamber HPDC cell on a 400-600 t machine typically runs 60-180 second cycles, hitting roughly 500 parts per hour. Wall thickness under 3 mm and proper vacuum-assist shave the longest stage, solidification, by 20-40 percent.
For a large aluminum structural part, target a die casting machine in the 1,600-2,000 ton clamping force band; machine tonnage equals injection pressure ratio times total projected area times a 1.1-1.3 safety factor, so a 9,000-ton UH9000-class giga press is only justified for single-piece BEV body
For non-heat-treated structural HPDC parts, AlMg5Si2Mn delivers up to 40% weight reduction over AlSi10MnMg with naturally hard ductility, while AlSi10MnMg needs T6 heat treatment and vacuum casting to reach equivalent strength, creating a clear choice between ductility-without-heat-treatment and str
Mold base steel prices move on a base-plus-alloy-surcharge model, with the surcharge tied monthly to nickel, chromium, molybdenum, manganese and iron. For pre-hardened, through-hardened and stainless mold base grades, the surcharge is typically the swing factor that flips a 30-90 day quote from in-b
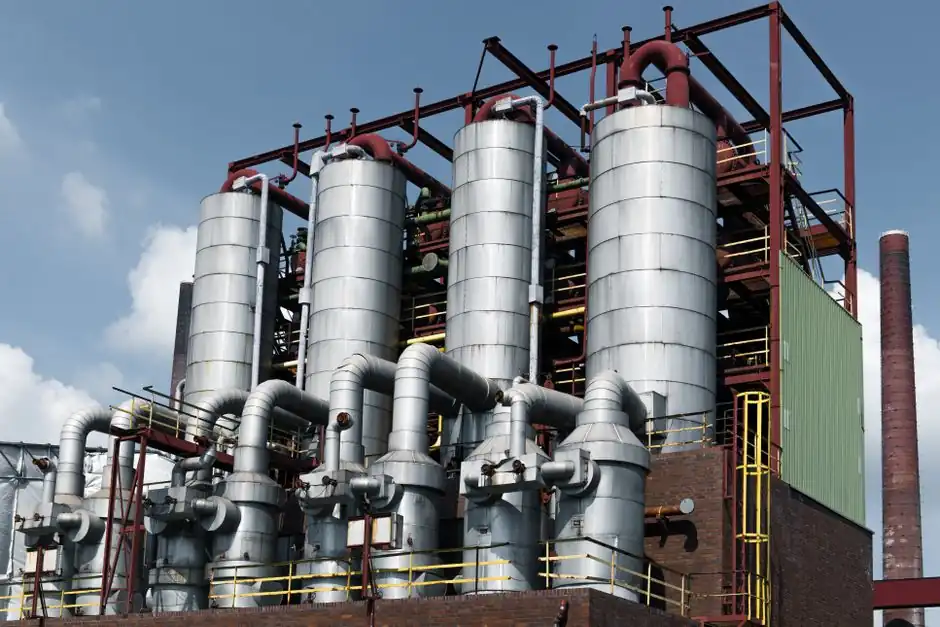
Fluidized bed sand coolers typically run a 1.6-2.2% outlet moisture with +/-0.2% accuracy and handle inlet sand above 150 C using evaporative water sprays on a vibrating, air-permeable deck, with airflow chosen to fluidize the bed rather than carry fines.
Water-mist cooling cuts low-pressure wheel casting cycle time and die peak temperature versus compressed air, with published data showing peak die temperature dropping from 574°C to 538°C at 0.30 MPa air / 0.38 MPa water. Air-only cycles stay around 5 minutes per wheel; water-mist and internal water
For gravity die casting dies, water circuits, bubblers, baffles, jet coolers and internal spray cooling each address different heat-extraction needs. Choose circuits for general cooling of large simple sections, bubblers for spot-cooling thick areas, baffles where space is tight, and jet or spray sy
For shop-air pre-compaction or air-impact work ahead of a static-pressure squeeze cycle, target 120 PSI static at the regulator so working pressure at the tool holds 90-100 PSI, with 3/8 in. hose minimum and a compressor sized to 130% of the thirstiest tool's CFM.
Compressed-air aftercoolers paired with moisture separators are the lowest-cost way to stop caking, clogging, and "chugging" in abrasive blast pots, with skid units sized from 300 to 800 CFM routinely hitting air within 10 °C of ambient.
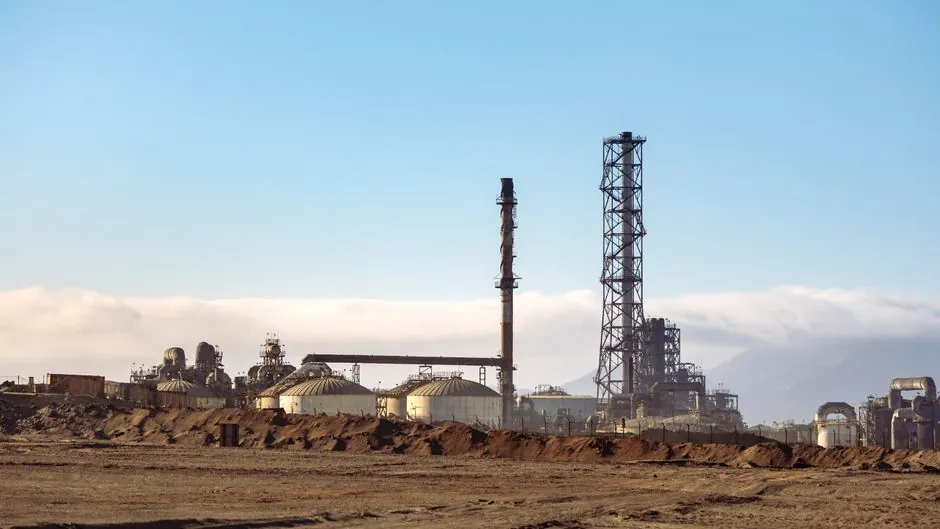
Thermal sand reclaimer afterburners oxidize VOC and odor from binder burnout at 1350°F or higher, with combustion chambers insulated to 650–750°C for sub-1 s residence time, and TOC outlet targets of 30–50 mg/Nm³ on coated sand streams.
For fine-detail shell molds, specify AFS grain fineness of 100 or higher using resin-coated silica sand, with finer zircon reaching 150 for tightest tolerance work. AFS 50–70 base silica coated with 1–2 wt % phenolic resin is the standard formulation, paired with 0.5–3.0 % calcium stearate release a
AFS Grain Fineness Number (GFN) inversely indexes silica sand grain size for foundries, with GFN 30-40 (0.6-0.8 mm) favoring steel castings and GFN 50-70 (0.3-0.6 mm) producing finer cast surfaces.
AE44 (Mg-4Al-4RE) and AS41 (Mg-4Al-1Si) are both creep-resistant magnesium die-casting alloys, but they solve the problem differently: AE44 relies on Al-RE intermetallics and age-hardening with Mn, while AS41 uses Mg2Si skeletons. Specified at 150-175°C powertrain service, AE44 generally leads AS41
For outdoor die cast housings, A413 aluminum offers better pressure tightness, higher fluidity for thin walls, and a corrosion-resistance edge over A380 per NADCA guidance, while A380 (ANSI/AA A380.0) remains the default for its balanced strength, cost and castability. Choose A413 when leak-tight th
A383 is the thin-wall variant of A380: higher silicon (9.5–11.5% vs 7.5–9.5%) gives better die fill, while A380 wins on strength (UTS 324 vs 310 MPa) and hot-tear resistance on thicker, structural parts.
A-shape crucibles suit stationary pit and induction drop-coil lift-out furnaces, while B-shape flat-bottomed and spouted/bilge crucibles are the standard fit for tilting furnaces where metal pours by gravity. Selection is dictated by the support/seat geometry, the lift mechanism, and the spout or po
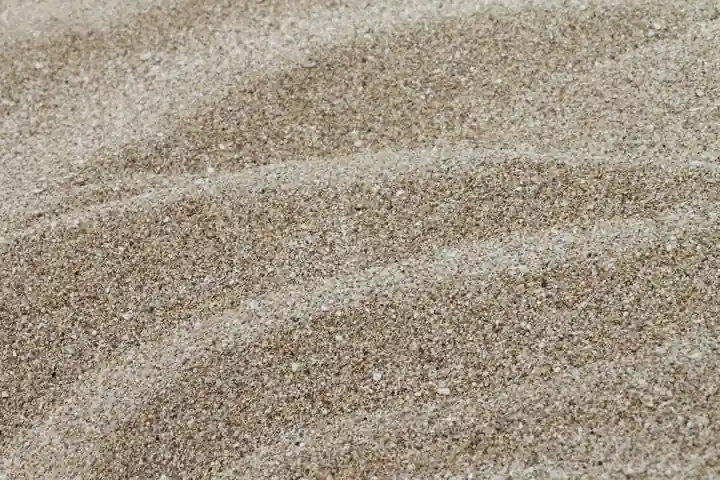
Aluminum sand molds typically use AFS 50-100 fineness (around 100-200 µm) while steel castings use AFS 25-45 (300-600 µm), because aluminum pours at 1,250-1,400°F and needs finer grains to control surface finish, gas permeability, and burn-in, whereas steel at 2,850-2,950°F demands coarser sand for
80 m/s fettling wheels deliver roughly twice the peripheral surface speed of 50 m/s wheels, raising MRR but also tripling burst-stress risk if the machine is not matched. Choose 80 m/s only for rigid, high-horsepower floor stands rated and balanced for it; stay at 50 m/s or below for portable, light
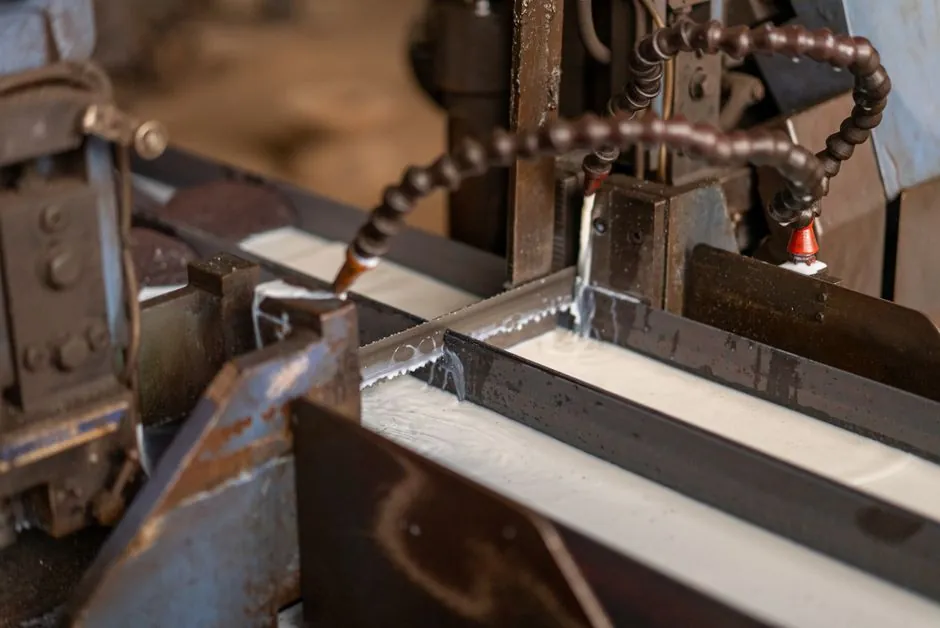
Mold base steel typically costs $2.00-$12.00 per kg depending on grade (P20, S50C/S55C, H13), with a complete A-Series mold base in D-M-E #3 steel running $4,000-$15,000 fully machined. Cost drivers are steel grade, plate count, frame size, and tolerance, not raw kg price.
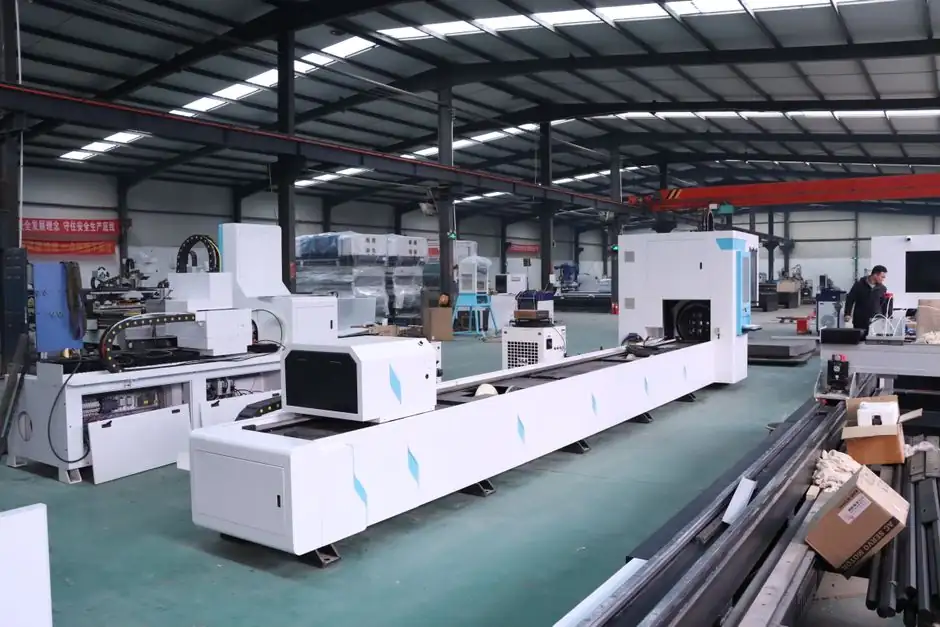
ZA-27 and ZA-12 zinc-aluminum alloys must be cast on a cold chamber die casting machine because their ~25-28% aluminum content and melt range of 375-484 degrees C cause iron attack on cast iron melt equipment, a failure mode that hot chamber cast iron goosenecks and plungers cannot survive.
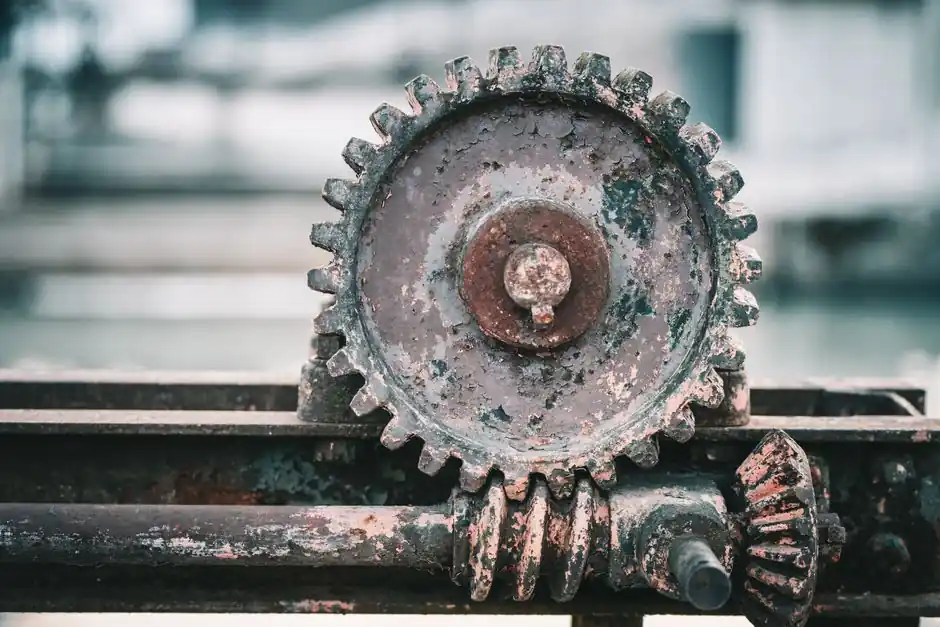
A foundry pouring ladle gearbox must be dynamically self-locking so that a tilted ladle full of molten metal cannot free-fall when the operator releases the hand wheel or if the drive stops. DIN EN 1247 (C-standard) requires a brake spring / load-torque lock that holds output torque even with applie
Sodium silicate bonded sand resists reclamation because the inorganic binder film does not burn out during pouring, leaving a tenacious silicate skin on each grain; wet-reclamation pilots now report 98% contaminant removal and 95% new-sand replacement, while thermal processes still consume 13-16 m³
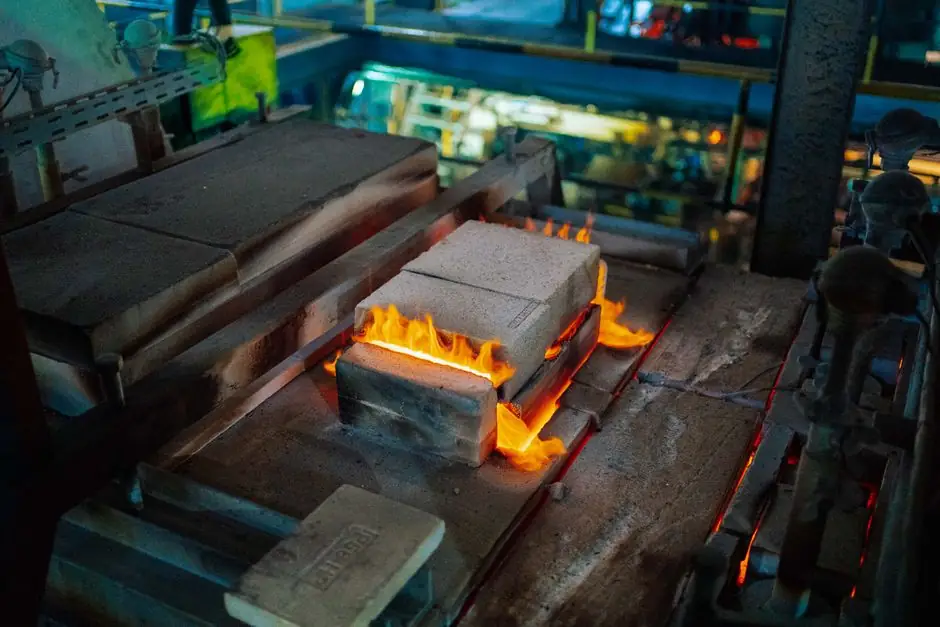
Fuel-fired crucible furnaces routinely post thermal efficiencies in the 12% range, with some setups losing up to 88% of burner input, because heat must conduct through a refractory crucible wall instead of contacting the metal directly. Wasteful factors stack: small charge size, hot flue gas, shell
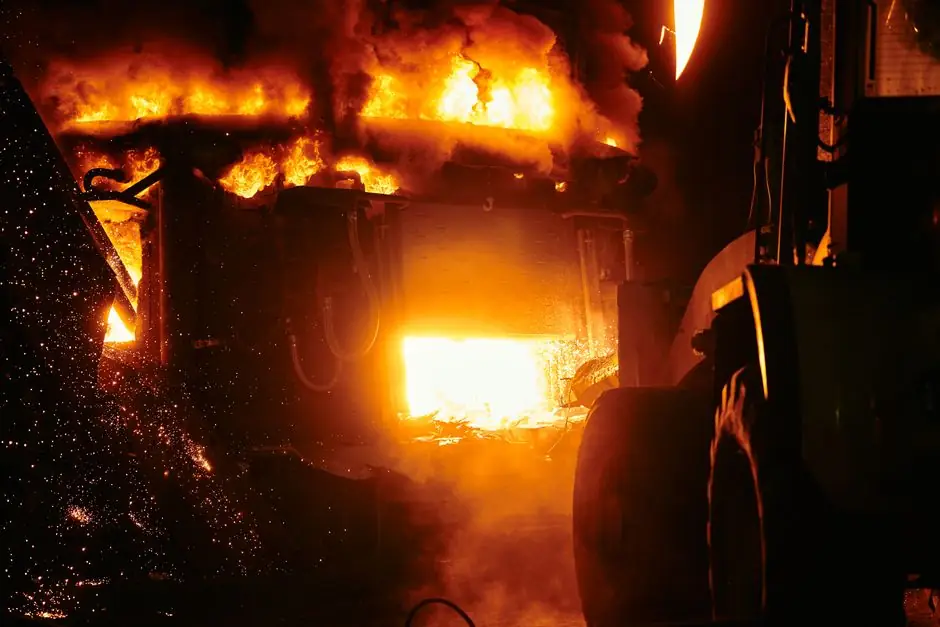
A cupola furnace is locked to cast iron because its coke-fired shaft tops out near 1,700 °C with high carbon and sulfur pick-up, which is exactly what gray and ductile iron need but is fatal to low-carbon steel chemistries and most non-ferrous alloys.
Silica sand causes rattail and scab defects through quartz thermal expansion, especially the reversible alpha-beta transformation at 573°C that generates compressive stress in the mold surface. Low wet tensile strength and low-deformability bentonite allow the heated shell to buckle or break off int
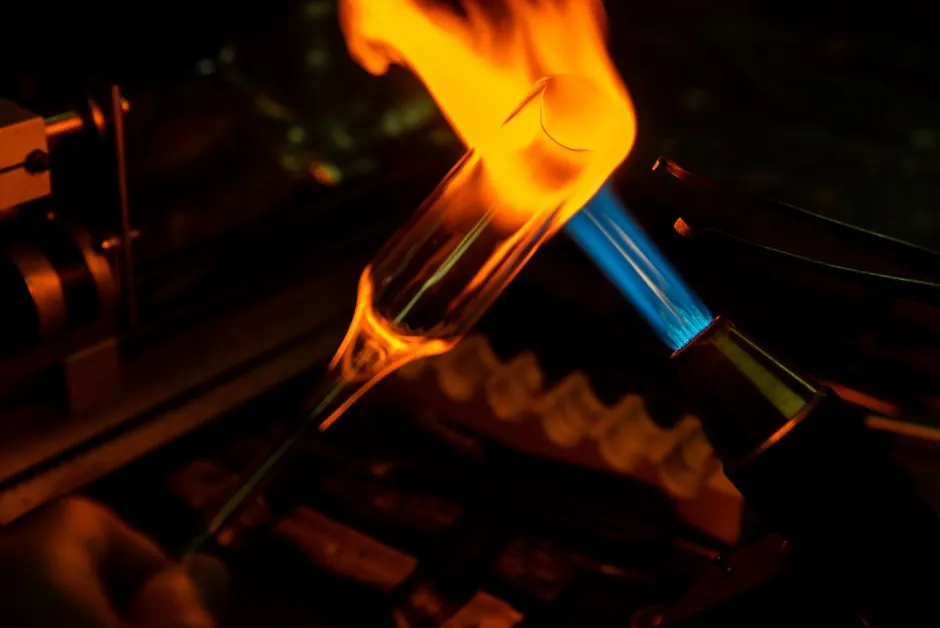
A channel-type induction furnace needs a permanent molten heel because the molten loop in its inductor channel acts as a single-turn short-circuited secondary winding of a transformer, and without that liquid metal loop the induced eddy-current path simply does not exist.
Channel induction furnace inductor channels clog because iron oxide-based spinel clusters nucleate on colder refractory walls and grow as a ceramic-like deposit, restricting molten metal flow and electrical efficiency.
Hot box cores turn brittle when the core box runs above ~550°C because phenolic/furan resin burns off, leaving a carbonised, over-cured shell that fractures under handling and pouring stress.
A squeeze pin should fire after the cavity is sealed by the freezing gate and while the target mass is still in the semi-solid state: 1.5–3.5 s after the high-shot changeover position is a working window, with 1.5 s typical. Actuation must be tied to local solidification, not the cycle clock.
Cold box core blowing and core shooting are not interchangeable: blowing fills a hot core box with free-flowing resin-coated sand at 0.2-0.4 MPa, while shooting propels mixed sand-binder at high velocity into a clamped cold box. Use this rule to pick equipment for PU cold box, Croning shell, and hot
Sand sintering point is the lower edge of a molding sand's fusion range, and it controls whether the aggregate resists burn-on at molten-metal temperatures. The 1928 Bureau of Standards test places that onset between roughly 1000 °C and 1500 °C true temperature, with silica, chromite, zircon, olivin
Charge hanging and bridging in a cupola shaft are caused by oversized scrap geometry, uneven burden distribution, low melting-zone temperature, refractory build-up, and tramp-element accretion, and are typically resolved by enforcing a maximum 1:3 charge-to-shaft-diameter ratio and a stable 8-12 per
Blast furnace and cupola operators are pairing high-accuracy magnetic flow meters (0.15% of reading) on tuyere inlet and outlet circuits with AI-driven thermal analytics to detect copper tuyere leaks down to a few drips per minute, replacing run-to-failure schedules. Reference sites use a 150 L/hr d
Warm Box and Hot Box core making differ mainly in curing mechanism and core-box temperature. Hot Box hardens cores inside the box at 180 to 240°C without catalyst, while Warm Box uses a pre-warmed box that starts curing and finishes outside, typically with a catalyst.
Vibrating shakeout machines (two-mass and barrel-horse designs) and rotary shakeout drums split cleanly on casting fragility, sand-to-metal ratio, and dust control needs. Use vibratory drums for no-bake, brass, and high-throughput (up to 400 TPH) lines where casting damage must be minimised; use rot
Vertical squeeze casting machines force molten metal into the die at 0.1–1.0 m/s under 50–150 MPa intensification, producing near-zero porosity parts; horizontal cold-chamber die casting injects at 1–10 m/s under 7–350 MPa for high-volume thin-wall output. Choose vertical squeeze for safety-critical
Vertical squeeze die casting injects molten aluminum upward (or downward) with direct intensification pressure, producing near-zero porosity parts for structural castings, while standard cold chamber high pressure die casting (HPDC) uses horizontal shot sleeves at 7-350 MPa for high-volume thin-wall
Cold-box core vent area should run 1.5 to 2.5 times the total blow-hole area to avoid blowholes and low-density scrap, with vent style opening rates from 13% slotted to 43% Shalco Super Vents.
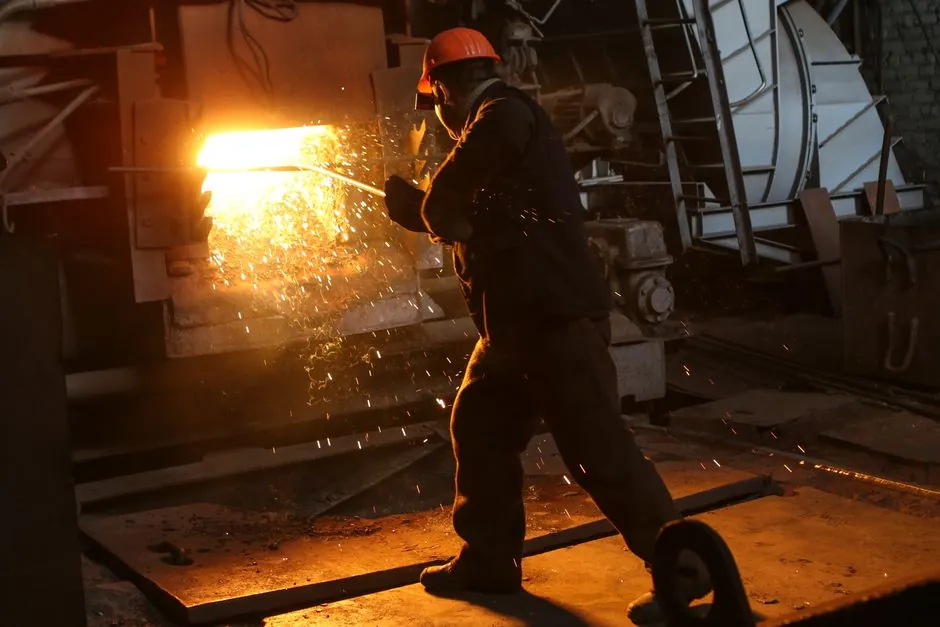
Vacuum induction melting (VIM) is the correct primary process for nickel- and cobalt-based superalloys containing Al, Ti, B, and Zr, while air induction furnaces stay relevant for non-reactive ferrous melts. VIM delivers oxygen below 20 ppm, nitrogen below 10 ppm, and Ti/Al control within ±0.05–0.12
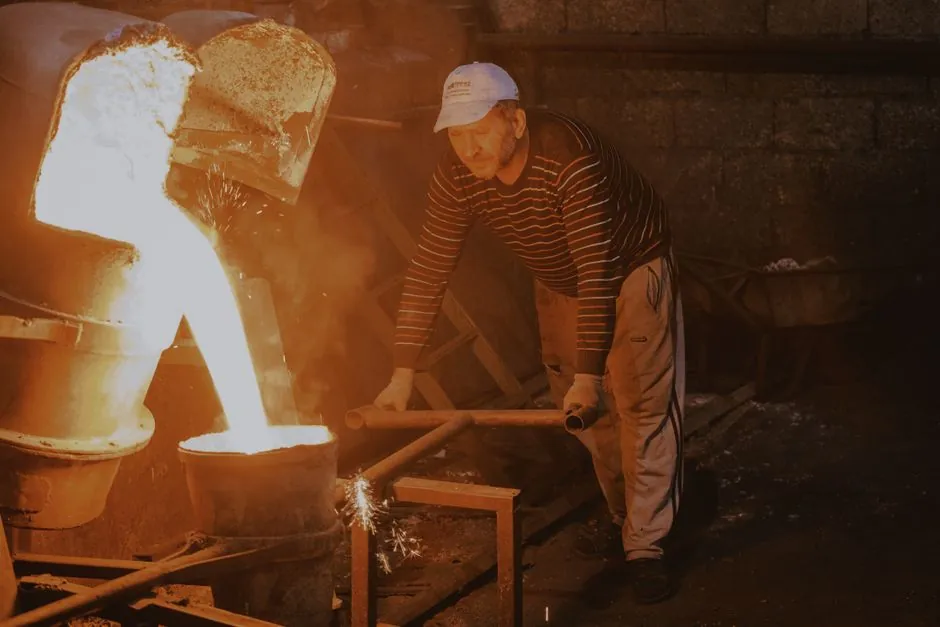
VD (ladle tank degasser) and RH (Ruhrstahl-Heraeus circulation degasser) target the same goal: dropping hydrogen, nitrogen, and carbon in liquid steel, but they diverge on heat size, circulation, and steel-grade fit. RH circulation units process 20 to 40 heats per day at 30 to 60 t/min through the v
A two-piece shot sleeve with a replaceable pour-zone insert is built as three parts: a sleeve body, a replaceable bushing under the pour hole, and a locking flange. AISI H-13 / 1.2344 at 44-48 HRC remains the standard tooling, with thermoregulated and integral-liner variants extending service life 2
Tilting shot sleeve docking on a vertical squeeze casting machine combines a vertical shot sleeve with a tilt-mounted pour cup, keeping molten metal at temperature, shortening pour-to-inject time, and supporting pressures near 1 ton through solidification. The configuration suits aluminum and magnes
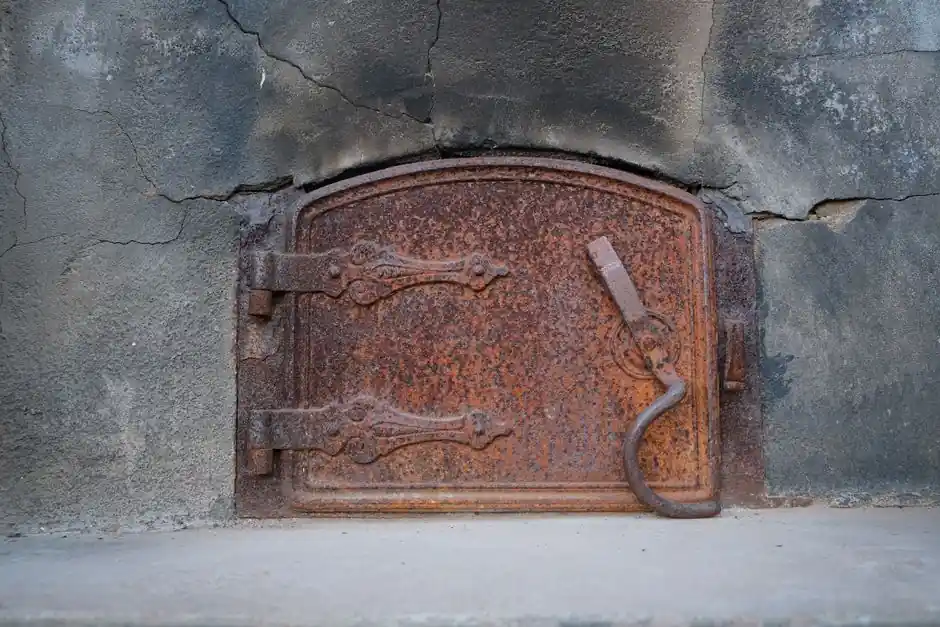
Tilting holding furnaces are now the standard metal-delivery workhorse for vertical direct-chill aluminium billet casting, replacing stationary vessels to improve drain-cleanliness, alloy-change speed, and launder control. Capacities of 50-100 t/charge and natural-gas regenerative firing dominate ne
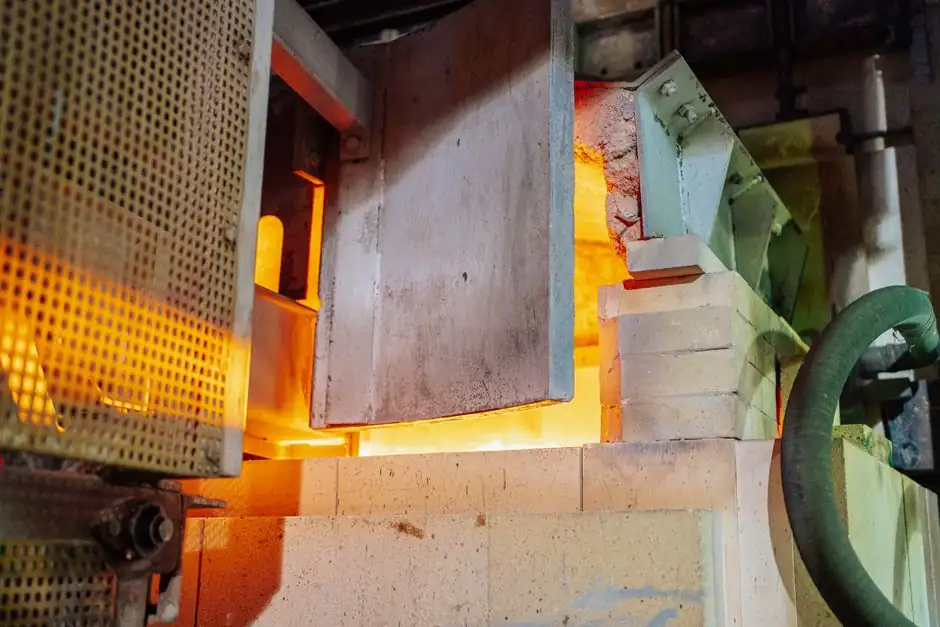
Tempering ovens cover roughly 300–1050°F (150–565°C) with forced-air convection and ±10°F uniformity, while heat treatment furnaces reach 1400–2300°F with controlled atmosphere or vacuum for hardening, annealing, and carburizing.
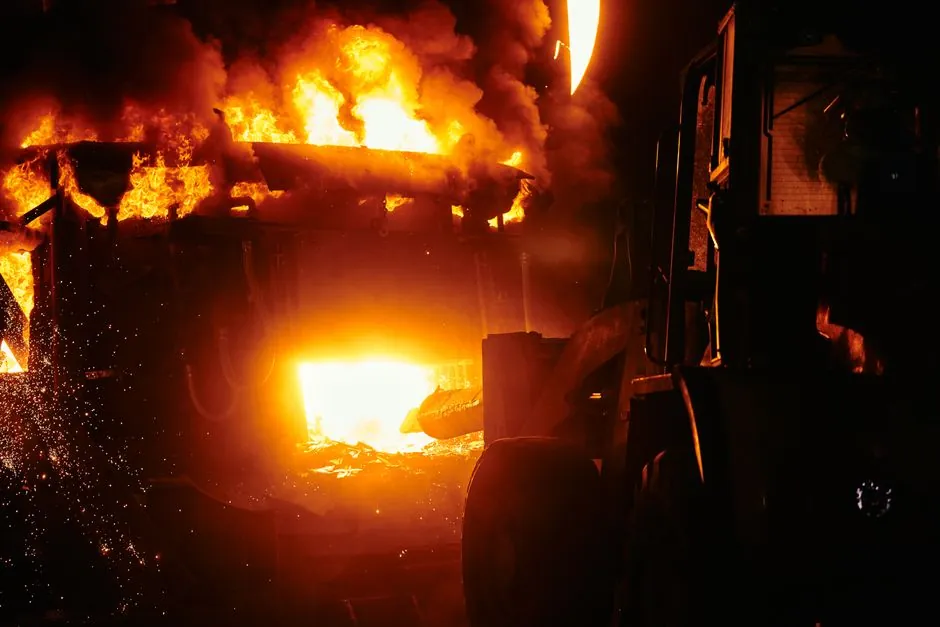
Bottom-pour ladles with monoblock stoppers dominate steel-foundry production above 500 kg for zero-slag pouring and lower maintenance, while teapot ladles remain the default for steel investment casters below 500 kg where stopper preheating is impractical. The decision is driven by capacity, slag co
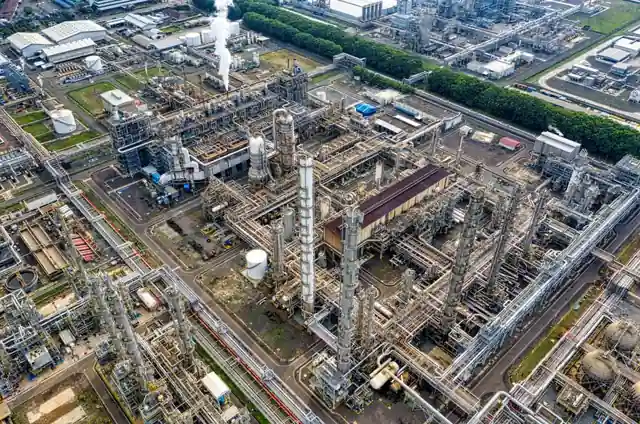
For amine regenerator off-gas, sulfuric acid scrubbing and thermal oxidation are competing abatement routes, not equivalents: acid scrubbing recovers the sulfur as a saleable product from concentrated H2S, while thermal oxidation at 760-982 degrees C converts H2S to SO2/SO3 that must then be neutral
Cupola furnaces remain the workhorse for stone wool melting with ~50% thermal efficiency and short start/stop cycling, but electric melters are displacing coke-fired units to cut CO2; selection hinges on capacity (1.5–12 t/h), fuel cost, and waste-feed flexibility.
Standard catalog mold bases ship in 1 to 5 business days and dominate tooling economics, while custom mold bases start at a 5-day lead time before any machining backlog. Buyers should default to catalog sizes from 7.875 x 7.875 in to 24 x 35 in unless geometry forces a custom plate stack.
For die-casting fettling, round cast aluminum shot (0.6–0.8 mm) is the default for zinc parts, cast zinc shot (ZA4, 90 HK) suits aluminum deburring with low dust and low explosion risk, and stainless cut-wire shot wins on cleaning efficiency and consumption. Match media to substrate hardness, ferrou
Hydraulic squeeze pins solve shrinkage porosity in HPDC but introduce a parasitic failure mode: seizure and bore galling inside the die. The same flash and lubricant that buy pin life also contaminate feed paths, and the fix is mechanical, not chemical. A typical HPDC cell running four to eight pins
Squeeze pin diameter for HPDC boss porosity typically lands in the 10-12 mm range, with stroke sized to match the local shrinkage volume measured at the hot spot, and actuation timed to fire as the metal passes through a critical solid fraction near 0.7. Choosing pin diameter, stroke, force, and act
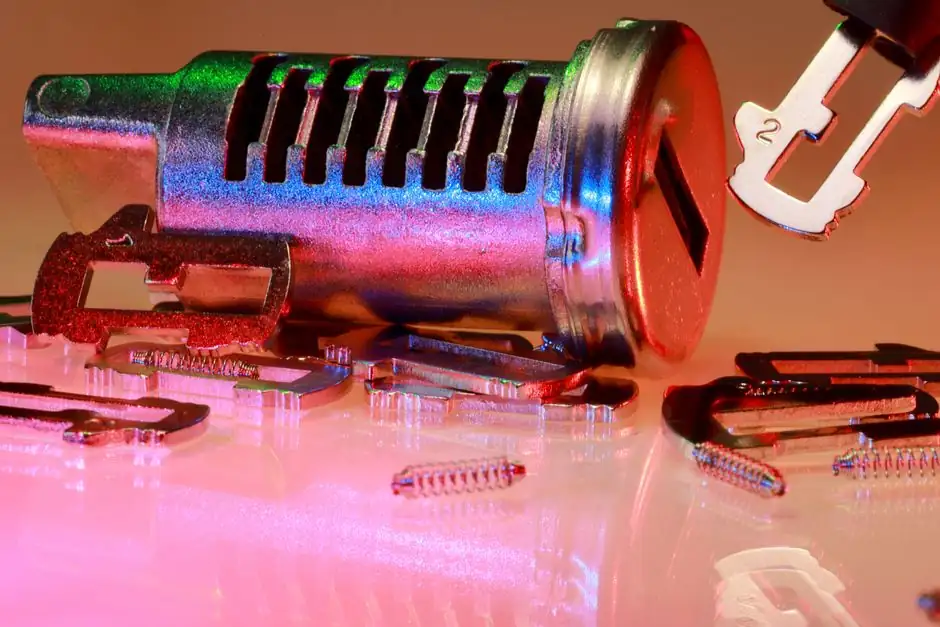
Squeeze pins are hydraulically actuated local intensifiers that press into solidifying aluminum during HPDC to cut shrinkage porosity in thick sections where the main shot piston can no longer feed. Effective design depends on pin placement, stroke, timing window, and intensification pressure, and i
For porosity and mechanical strength, squeeze casting delivers near-zero internal porosity and T6-compatible strength, while HPDC wins on cycle time and thin-wall geometry. Spec HPDC for cosmetic high-volume housings; spec squeeze casting for fatigue- and pressure-loaded structural parts.
Squeeze casting clamping tonnage is sized from projected area times intensification pressure, with machine intensification ratios commonly 7:1 to 15:1 and direct squeeze presses typically rated 800-8000 t for aluminum structural parts.
Squeeze-cast A356-T6 reaches 290-310 MPa tensile with 8-12% elongation and sub-1% porosity at 50-150 MPa applied pressure, while gravity die-cast A356-T6 typically lands near 220-260 MPa tensile with 3-5% porosity, so squeeze casting wins on fatigue-critical structural parts when tooling cost is jus
Small cupola furnaces for job shop foundries typically deliver 0.5 to 5 metric tons per hour, with internal diameters from 0.5 m to roughly 1.5 m and melt zones 3 to 6 m tall. Selection hinges on batch size, charge mix, and whether the operation runs continuously or in intermittent shifts.
Skin drying uses torches, radiant lamps, or electric elements to dry only the cavity face of a green sand mold, typically 0.5 to 1 inch deep, producing a dry-sand-class surface on a green-sand-class backing. It is specified for medium to heavy iron and steel castings where surface moisture must be r
Silicon nitride (Si3N4/sialon) protection tubes deliver >99% thermal efficiency in aluminum holding furnaces versus 20-45% for gas-fired top heating, with typical service life of 12-24 months versus 4-8 months for silicon carbide. SiC radiant tubes win in higher-temperature air-service applications
Silicon carbide briquettes added to a cupola charge deliver three foundry functions at once: Si and C recovery, melt deoxidation, and partial coke replacement, with commercial grades spanning 36% to 80% SiC at typical 4.5-30 lb slab or cube sizes.
Silica sand remains the default low-cost casting aggregate, but for steel, stainless, and high-temperature alloys, chromite sand and zircon sand deliver the refractoriness, low thermal expansion, and chilling action silica cannot match above 1500 °C pours. Selection pivots on alloy pour temperature,
Aluminum cold-chamber die casting runs at 40-60% shot sleeve fill in practice, with 60% as the published optimum and 50-70% as the safe design band. Higher fill cuts air entrapment and thermal loss; lower fill risks turbulence and oxide inclusions.
Non-ferrous die castings (Al, Zn, Mg) are best finished with a centrifugal wheel blast system running non-ferrous or stainless media sized 0.4-2.0 mm, paired with a flash-removal screen; cut-wire steel, cast zinc, and zinc-aluminum cuts at 91 Knoop cover flash, deburr, and cosmetic finish without co
No-bake foundries typically reclaim 70–95% of spent chemically bonded sand, with the figure governed by binder chemistry, attrition intensity, and downstream LOI targets. Pneumatic and mechanical attrition systems routinely hold reclaimed sand LOI near virgin 0.3–1.5% and return grains to 0.15–0.6 m
Sand reclamation in modern foundries follows a six-stage mechanical-and-thermal sequence: shakeout and tramp-metal removal, lump crushing, attrition scrubbing, screening and air classification, optional fluid-bed calcination at 600-800 °C, then cooled return to the mixer silo, routinely reclaiming 9
Silica-based sand molds are rated for refractoriness up to roughly 1,650-1,820°C (3,000-3,330°F), and steel foundries pour within that window by relying on refractory sand systems, additives, and facing sands rather than the base silica alone. Above that envelope, the binder fails long before the si
Green sand and no-bake (air-set) sand casting both use silica grains, but green sand bonds with bentonite clay and water while no-bake bonds with a phenolic urethane resin hardened at room temperature. The result: 500 vs 20-30 molds per hour, 40-50% lower defect rates in no-bake precision work, and
A sand casting mold is built from three coupled systems: a cope and drag flask pair, sand cores for internal cavities, and a gating network that feeds molten metal from sprue to runner to gate.
Radiant tubes isolate combustion from the work, hitting 1,400°F to 2,100°F with 60 to 80 percent radiative transfer and 15 to 30 percent energy savings. Direct fired furnaces skip the tube, cut capital cost, but expose steel castings to oxidation and decarburization. Choose radiant tubes when surfac
Pressure pour channel-inductor holding furnaces let foundries store, superheat, and dose molten cast iron for molding lines, with typical holding-plus-pouring energy of 150 to 230 kWh/t on top of 510 to 550 kWh/t for melting at about 1450 °C, per OTTO JUNKER process data. Sealed-vessel designs
In a die casting cell the melting (pouring) furnace converts solid charge to liquid and the holding furnace stabilizes alloy temperature near the machine. Layout, sizing, and energy source choices for the two units directly control shot weight consistency, dross rate, and defect levels in HPDC and L
For very large castings above roughly 10 metric tons, pit molding handles size, depth, and floor-pit capacity while flask molding handles precision, handling, and repeatability. Hybrid flask-plus-pit layouts, like the 18-ton HT300 crossbeam case, are the practical answer when tooling and pit dimensi
Permanent mold, die casting, and sand casting differ most clearly in mold material, surface finish, and production volume thresholds. Sand casting uses expendable bonded sand molds with 300-900 RMS finish, permanent mold uses reusable steel molds at 200-420 RMS, and die casting uses high-pressure st
Parting powder is dusted onto green-sand patterns and along the cope/drag parting line to keep damp bentonite-bonded sand from sticking to the pattern and fusing the two flask halves together. Standard choices are dry silica, talc, graphite, and non-silica talc blends, each with different trade-offs
Shot blast recipes for die cast parts are tuned by part family and alloy: aluminum thin-wall housings get fine steel/glass bead at 4–6 bar to preserve surface finish, zinc die castings use softer media at lower pressure to avoid edge rounding, and structural high-integrity castings tolerate aggressi
For pre-hardened mold base plates in plastic injection tooling, P20 (DIN 1.2311/1.2738) at 280-320 HB wins on polishability and weldability, while 4140 Pre-Hard at 28-32 HRC wins on free-machining, toughness, and supply cost. Match by application: P20 for the molding surface, 4140 for support/holder
Oxygen enrichment of cupola blast raises melt rate and tapping temperature, with documented production gains of 15–36% and coke savings up to 22%, but continuous use demands compensatory coke charging to control refractory attack.
Olivine sand beats silica sand for manganese steel castings because Mg2SiO4 does not react with MnO to form MnSiO3 burn-on slag, while SiO2 does. Trade-offs: olivine costs more, runs at pH 9 to 10, and needs paired sand reclamation to amortise.
For carbon steel castings, full annealing (furnace cool from 30–50 °C above Ac3) maximizes machinability and residual-stress relief, while normalizing (air cool from roughly 800–950 °C) delivers higher strength and finer grain. Pick normalizing for structural consistency, full annealing for heavy ro
For sand casting, green sand delivers the lowest tooling cost and highest throughput (up to 500 molds/hr on automated lines) but loosest tolerances (~±0.060 in), while no-bake (chemically bonded) trades cycle time for roughly 2x tighter accuracy and 40-50% lower defect rates on precision parts, and
40 CFR Part 63 Subpart EEEEE sets HAP limits for iron and steel foundry cupola metal melting furnaces, with existing major sources required to comply by April 23, 2007. EPA projects the rule cuts air toxics by about 580 tons per year and other pollutants by about 1,850 tons per year.
For visible cosmetic surfaces, specify AFS grain fineness number (GFN) above 60, with 80-120 GFN the practical working band; coarser sand below GFN 50 is reserved for non-cosmetic structural castings where permeability, not finish, drives the call.
Tie bar spacing sets the hard ceiling on mold base width and length inside any horizontal injection molding machine. Mold width must be at least 50-100 mm less than tie bar clearance, and a 4-cavity family mold is feasible only when both dimensions fit cleanly between the bars.
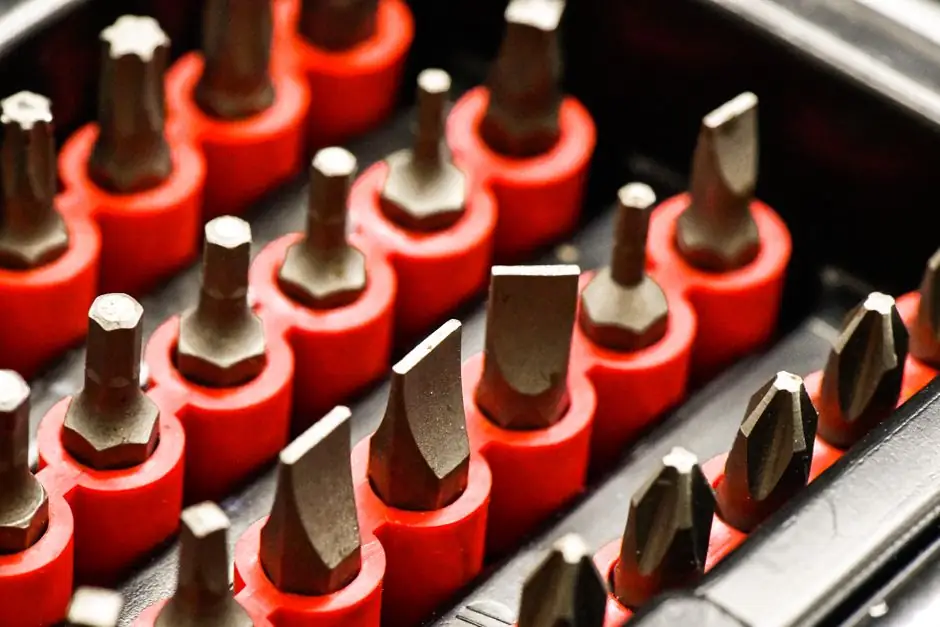
Standardized mold bases with interchangeable cavity and core inserts cut injection-tooling changeover from hours to minutes, with the mold base staying in the press while only functional inserts are swapped. Choose this architecture for low-to-mid volume, prototyping, and family part runs under roug
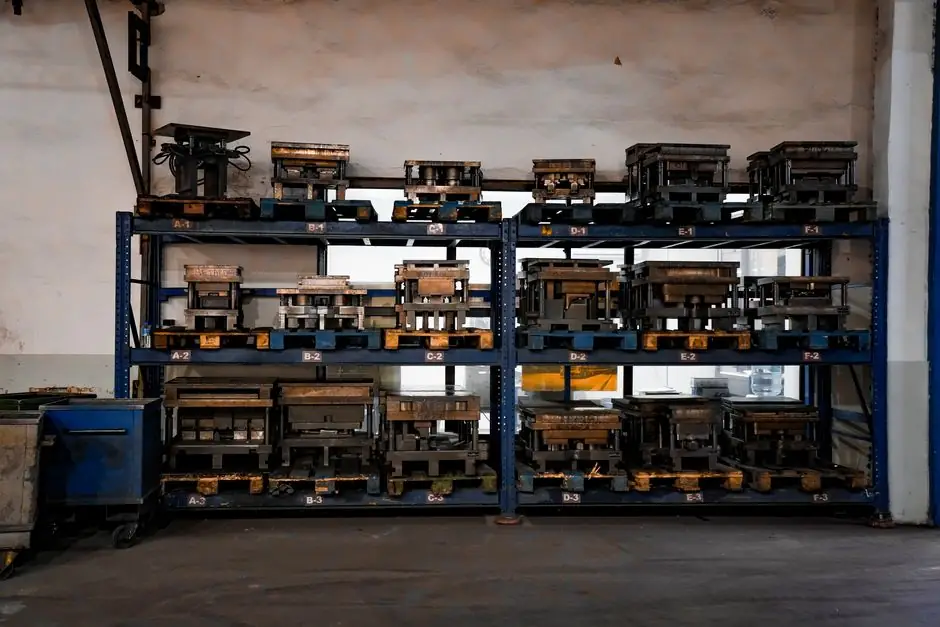
High-cycle injection molds typically run P20 family pre-hardened steel at 28-43 HRC for cavities and cores, switching to H13 or H11 at 48-52 HRC after heat treatment for abrasive or glass-filled resins above 500,000 cycles. Mold-base holders stay at 27-33 HRC (4140+S / 1.2331 class) for machinabilit
A DME-standard mold base frame is dimensionally interchangeable across A, B, AX, T, X and MoldBasics series, with the A-Series 7-plate stack-up covering footprint sizes from 7.875 x 7.875 to 23.75 x 35.5 inches and over 75 trillion configured assemblies. Cross-supplier plate interchangeability requi
Prototype mold base selection for runs of 100-10,000 parts pivots on aluminum vs soft-steel vs 3D-printed inserts, with modular frame systems and PM-F0 surface finishes cutting lead time to under two weeks. Match mold-life class to projected volume growth, not just the first batch.
For plastic injection mold base plates, P20 (pre-hardened 30-36 HRC, ~0.40% C, Cr-Mo) is the default for medium-volume, complex-cavity tooling where no post-machining heat treat is wanted; 1045 (medium-carbon, ~0.45% C) is the cheaper structural-frame and bolster choice when you weld, flame-harden o
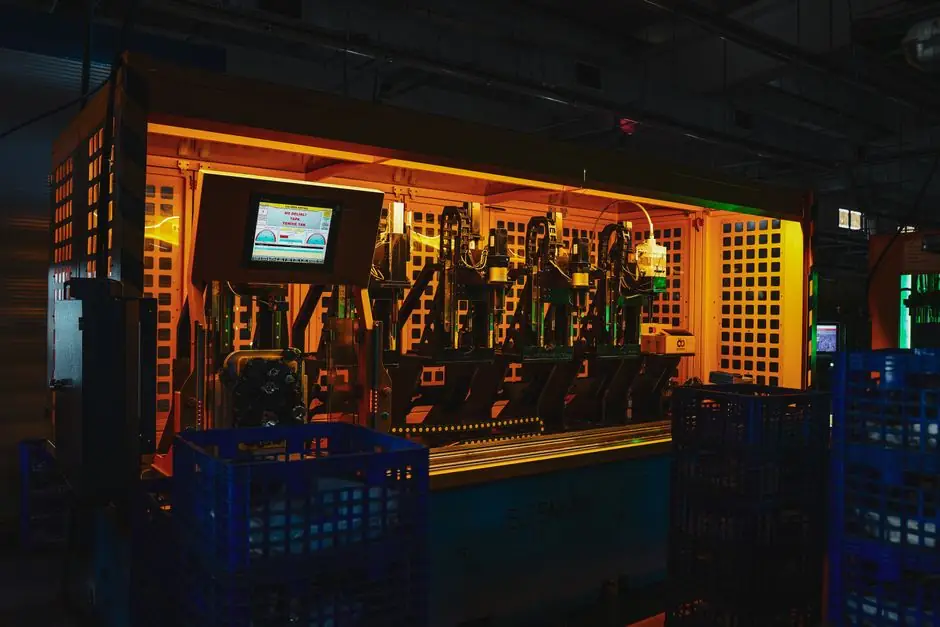
Medium die casting machines span roughly 250-800 metric tons of clamping force, suited to parts with projected areas around 200-800 cm² and shot weights of 1-10 kg. Tonnage = injection pressure ratio × projected area × safety factor, with a 1.1-1.3 safety factor typical for production runs.
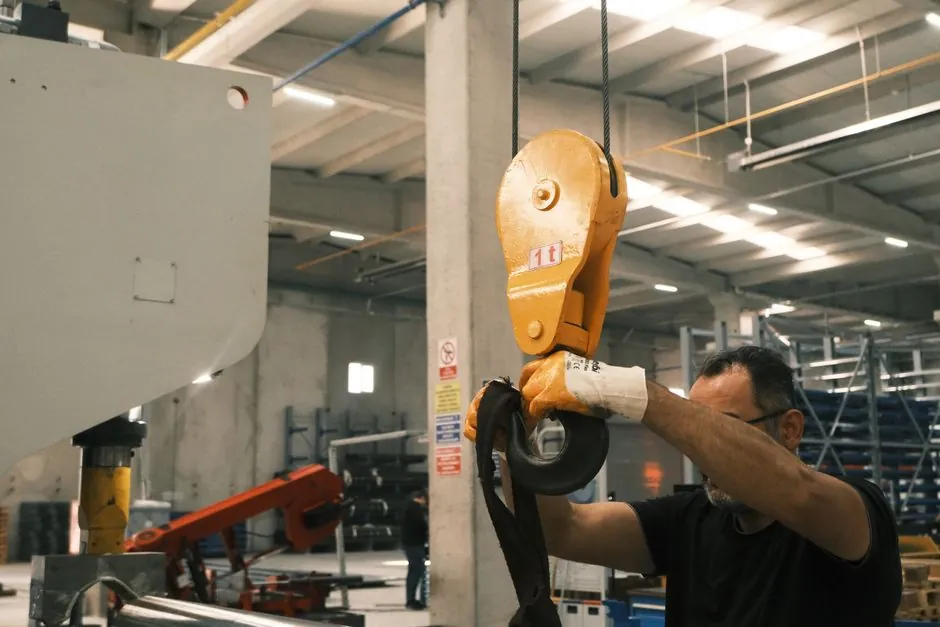
Medium die casting machines (roughly 400-800 ton clamping force) typically need 5-8 m of overhead crane hook height and 25-40 m² of floor footprint, including die change clearance, and these numbers must be matched to die weight and platen size before specifying a quick die change retrofit.
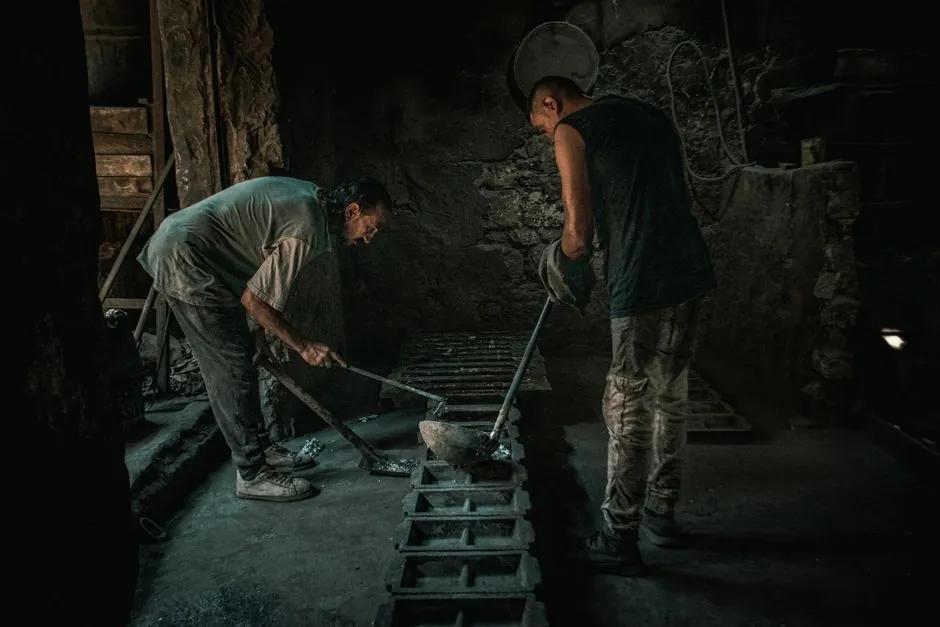
Manual gravity die casting machines start around $6,000 (Rs 5 lakh) for basic Indian-market units, while semi-automatic and fully automatic machines range from $150,000 to over $1.5 million depending on tonnage and features. The cost gap reflects labour displacement, cycle-time gains, and yield impr
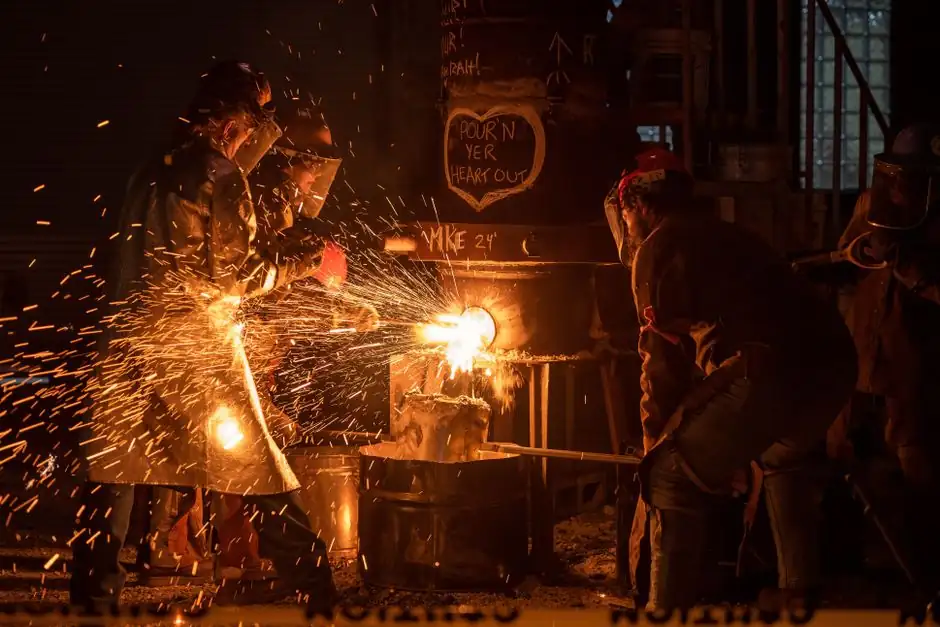
Magnesium in treated ductile iron held in a pressure pour furnace fades continuously: residual Mg typically drops toward 0.04 wt% within 12-15 minutes, forcing foundries to either pig the heel or refresh it with MgFeSi, Ni-Mg, or Fe-Mg briquettes. Stabilized inert gas covers and a ~10% lower target
Magnesium die casting cells require a dedicated protective cover-gas system because molten magnesium ignites above roughly 473°C in air; SF6, HFC-134a, and now low-GWP fluorinated or argon-based blends keep the melt inert, with vent-less hoods and ~12 utility feeds per cell (S5, S6, S8).
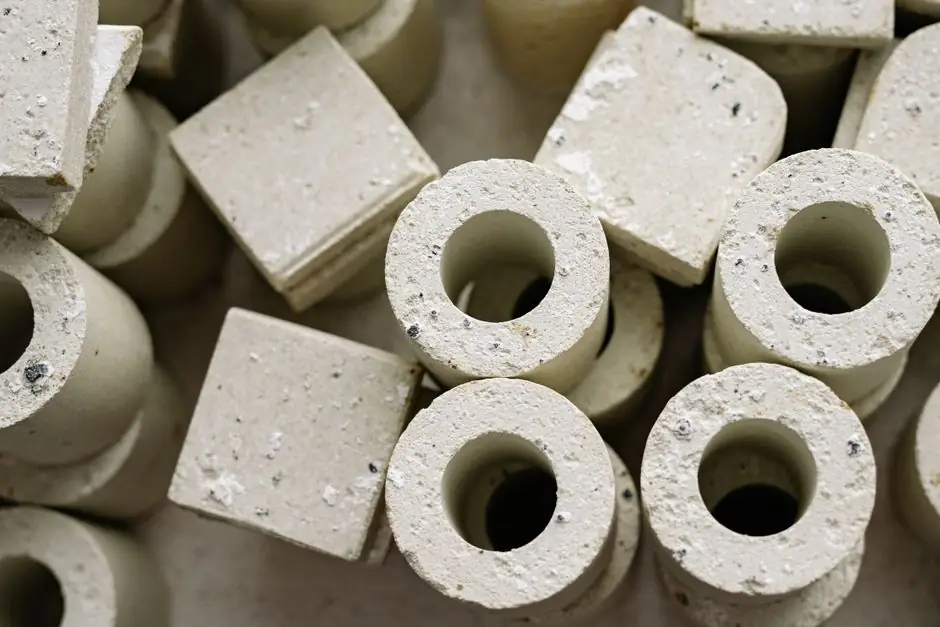
Loam molding remains the standard process for casting large bells and large cylinders where molding boxes and full patterns are impractical. The loam mix combines sand, clay, water, and organic fibers, shaped over a brick skeleton using a sweep pattern, then dried and fired before pouring bronze or
For lead-free brass faucet bodies, squeeze casting delivers higher density and lower porosity but demands controlled direct pressure; gravity die casting remains the lower-risk OEM baseline for complex sensor-ready bodies. Choose by part geometry, leak-test pressure, and lot size.
Lead-free brass for squeeze casting centers on three alloy families: bismuth-bearing (C27450/C2745), silicon-brass (CuZn21Si3P), and tin-bismuth-antimony (87.25Bi/12Sn/0.75Sb), with the 0.25% Pb threshold defined by US plumbing rules. Each family trades machinability, melt behaviour, and squeeze-pre
H13 and H11 are both 5% chromium hot-work tool steels, but H13's higher vanadium (0.80–1.20% vs H11's 0.30–0.60%) gives better hot-wear and heat-check resistance, while H11 wins on toughness and crack resistance for impact-loaded casting tooling.
An integrated shot blasting + trim press cell lines up deburring, flash removal, and surface finish in one robotic flow. Modern cells combine cold-chamber die casting, robotic extraction, hydraulic 4-column trim presses up to 150 t, tumble-wash with ceramic media, and conveyor-fed shot blasting, cut
Replacing resistance or gas-fired core-box heaters with medium-frequency induction cuts hot-box core-box warm-up to roughly 1-3 minutes, with shot cycles of 10-30 s at 180-250°C mould temperatures. The shift reduces idling energy, tightens cure control for phenolic, furan, and urea resins, and integ
Hydraulic, pneumatic, and manual die operation each suit different gravity die casting runs: hydraulics deliver 50-500 ton clamp force with PLC control, pneumatics cap at low tonnages under 50 tons, and manual setups fit prototyping below 1,000 units/year at 50-65% yield.
Aluminum holding furnace walls require daily hot cleaning to remove oxide buildup, with heavy production demanding up to three cleanings per shift; residential HVAC units only need annual service. Industrial aluminum furnaces (reverberatory and holding furnace types) follow a far stricter cadence th
Heat reaches the metal in a fuel-fired crucible furnace by three coupled modes: hot combustion gases sweep around the outside of the crucible and transfer energy to the wall mainly by forced convection plus flue-gas radiation; the refractory wall then conducts that heat inward to the inner skin; and
Furnace kW sizing for a heat treatment cycle comes from load weight, specific heat, target ramp, and endothermic soak, not nameplate kilowatts. The reliable shop formula is kW = (mass × Cp × ΔT) / (time × 3412) plus 10 to 30% losses, with hold-time drag from austenite transformation added separately
Hot box and cold box core shooter tooling cost diverge by process stage: hot box favors low per-shot tooling spend but higher energy, while cold box requires amine-gas equipment and PU resin tooling that raise initial cost but cut cycle time. Choose hot box for short runs and small cores, cold box f
Insulating the heated core box on a hot box core shooter can cut thermal losses from the 250–350°C tool surface and shrink per-core electrical draw, with the largest gains on long-curing-cycle cores where the 40–120 s dwell dominates the energy bill. Practical retrofits: ceramic-fibre blanket behind
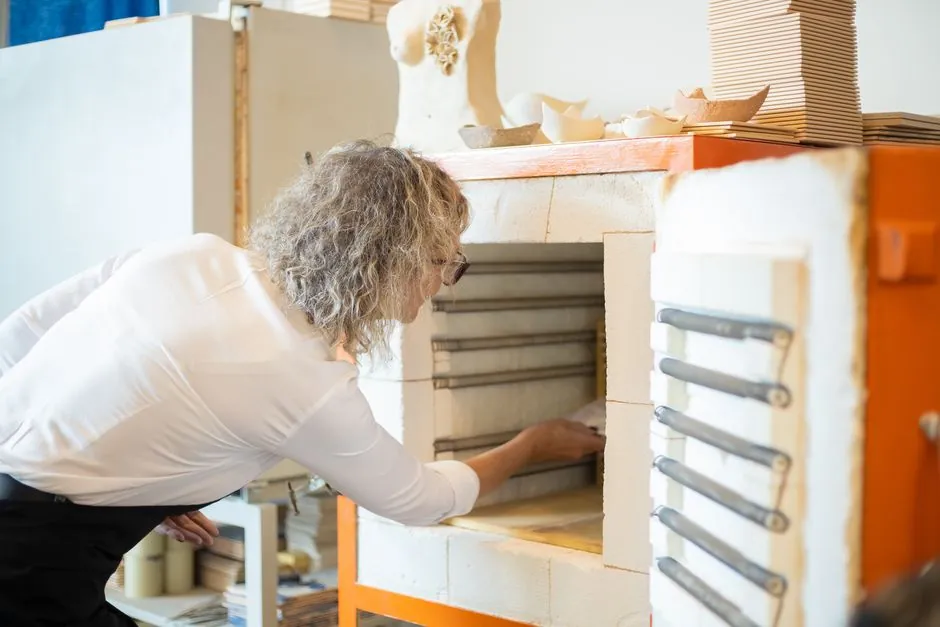
The Hot Box core-making process cures resin-bonded foundry sand inside a preheated core box held at 180-250°C, with phenolic, urea, and furan resins each tuned to different cure speeds and strengths.
Horizontal gravity die casting machines use PLC-managed interlock chains tying die-close, tilt, pour, eject and guard-door states together. Safety light curtains, dual-handed start, and position-confirmed mold close are baseline; servo tilt accuracy reaches ±0.05° on modern 4-column rotary cells up
For die-casting metal supply, holding furnace bath temperature should be held within roughly +/- 5 deg C of the target pouring set-point, using immersion thermocouples and closed-loop PID trim to stabilise shot weight, melt loss and alloy chemistry in HPDC cells.
Contact radar, laser triangulation and eddy-current non-contact level sensors are now the default choice for closed holding and dosing furnaces, with sub-millimeter accuracy and 1400°F (760°C) tolerance replacing legacy probe and ultrasonic designs in automated die-cast cells.
Integrating a holding furnace with an automatic ladle dosing system is achievable but loses 1-3% metal yield and roughly two-thirds more energy than a closed dosing furnace; dosing accuracy is typically ±1.5% in Westomat-style systems versus 3-5% in ladle dosing. Choose closed dosing for high-mix di
Heated mold bases for liquid silicone rubber (LSR) injection run cavity surfaces at 160-200°C with sub-±0.20 mm closure tolerances, using polished steel, integrated cooling channels, and tight thermal symmetry to vulcanize parts without flash.
A heated launder is the preferred molten aluminum transfer method between a melting furnace and a holding furnace, with single-line lengths commonly running 90-300 ft; transfer ladles remain the fallback for steel and for low-volume or layout-flexible aluminum cells.
Heated amine vapor generators and liquid amine injection differ fundamentally in V/L distribution, fouling tendency, and pH control band. Vapor feed favors pH 7.5-9.0 condensate chemistry for direct steam humidification, while liquid injection suits low-pressure scavenging but raises degradation ris
T6 solution treatment for aluminum castings runs at 500-550 °C (typically 530-540 °C) for 1-12 h, held within ±5-6 °C of setpoint and 10-25 °F below the alloy's eutectic, then water-quenched at 66-100 °C and aged at 154-227 °C to hit T6 mechanical targets of ~235 MPa UTS, 165 MPa yield, 70-105 BHN.
Hand-shank ladles cap at roughly 20 kg operator load for iron-pouring work, while geared crane ladles scale from 450 kg to 165,000 lb (75 t) on worm-and-wheel gearboxes. Choose hand-shank for short, low-temp, intermittent pours; choose geared crane for any job above operator limit, continuous duty,
For gray iron green sand molds, the operational target for green compression strength (GCS) is 1,800 g/cm², paired with permeability 130, moisture ~2.8%, and mold hardness 90. Permeability contributes 61.53% of casting-quality variance, GCS 21.54%, and pouring temperature 5.52%, defining the hierarc
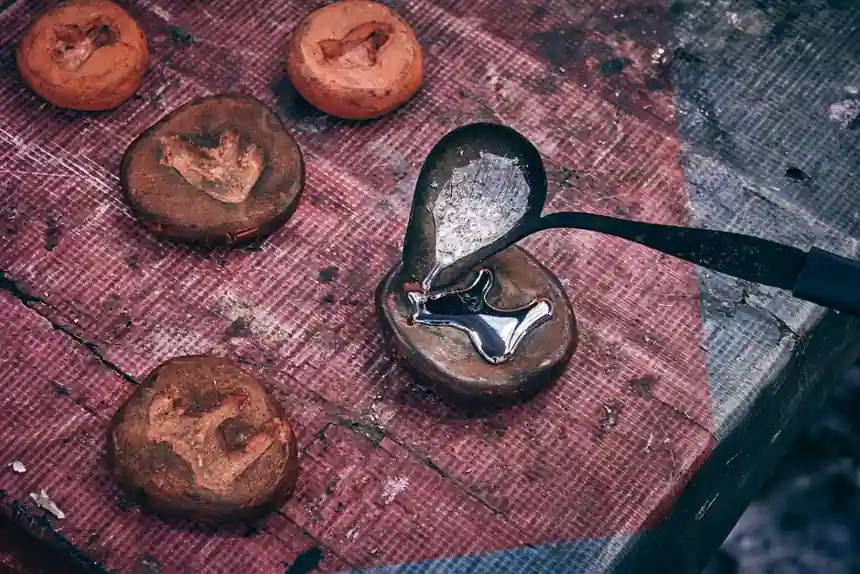
Gravity die casting breaks even against sand casting between roughly 500 and 5,000 parts per run, with GDC dominating the 1,000–50,000 unit band where sand casting quality is insufficient but HPDC tooling cannot yet be justified. Below 300 parts, sand casting wins on tooling cost; above 10,000 parts
Tilting gravity die casting machines fill the mould by rotating it from a near-horizontal pour position back to vertical, keeping the metal head low and the flow laminar. Tilting up to 90 degrees with PLC-controlled speed on 300 kN-class hydraulic platens is the standard configuration for gas-tight
Mid-tonnage gravity die casting machines in the 400-1000 ton clamping-force class typically run USD 120,000-350,000 for new units, with 660-1100 ton models commonly listed at INR 25-30 lakh (about USD 30,000-36,000) on the Indian subcontinent market; used 100-200 ton entries start near USD 80,000. T
Gravity die casting machine prices scale steeply with locking tonnage, ranging from roughly $50,000 for sub-50-ton bench units to over $1.5 million for 3500-ton giga-casting class presses. Cold-chamber aluminum setups at 800 tons cost around $600,000, with vacuum and automation packages pushing the
An entry-level gravity die casting line for aluminum runs roughly $80k to $250k all-in, with the machine, permanent copper/steel dies, melt furnace, trim press, and trim tooling the dominant cost lines. Pricing is driven by five levers: alloy, die complexity, clamping tonnage, annual volume, and pos
For aluminum high-pressure die casting, in-gate velocity of 30-50 m/s corresponds to fill times of roughly 41-69 ms in extra-large thin-wall parts, with below 30 m/s causing incomplete fill and 50 m/s producing complete castings. Industry guidance permits 25-60 m/s across thin-wall, structural, and
Gas-fired core box heating and electric cartridge heaters represent two distinct thermal delivery paths for foundries: combustion radiant/convective heating versus contact resistance heating at up to 1400°F (760°C). Electric systems convert nearly 100% of input energy to heat with lower maintenance
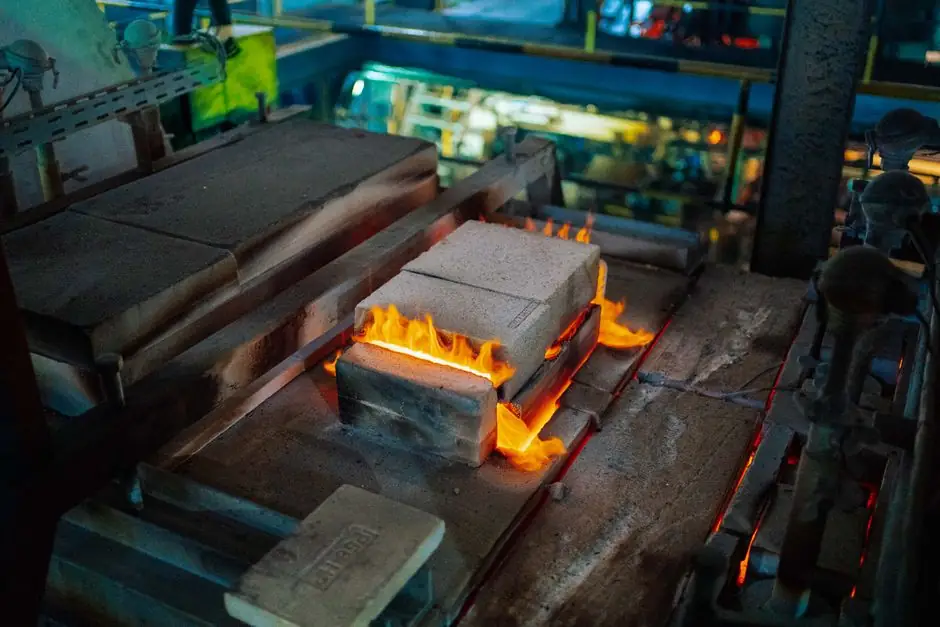
For hot-box cores, urea-modified phenolic delivers lower gas evolution, faster cure and longer bench life on iron/steel work, while furan-modified phenolic gives easier shake-out and smoother surface at the cost of more condensate. Selection is driven by alloy, pour temperature, and shake-out geomet
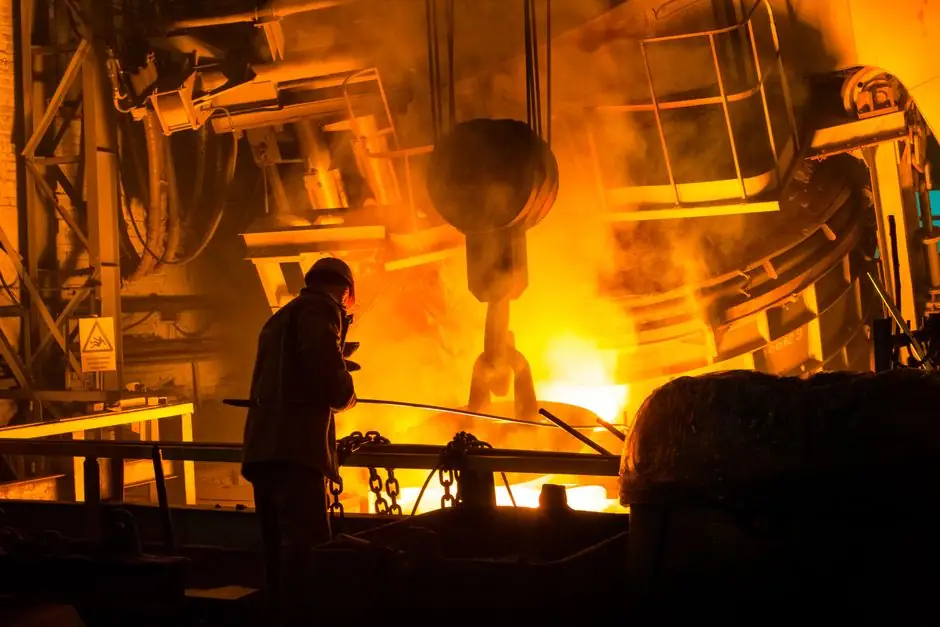
Foundry coke for cupola melting is specified at fixed carbon ≥88% min, ash ≤7.6–10% max, sulfur ≤0.5–0.95% max, moisture ≤2–5% max, and lump size typically 80–250 mm. Grade A delivers FC ≥90%, S ≤0.5%, ash ≤8% for high-grade iron; Grade B drops to FC ≥85%, S ≤0.75%.
Dry sand moulds for foundry casting are typically oven-baked at 300-650 °F (149-343 °C) for 8-48 hours, with moisture-control tests performed by drying sand to constant mass at up to 100 °C for about one hour. Time depends on mould size, binder, and oven airflow, while no-bake air-set systems intent

Dry sand molds are stronger, more rigid, and dimensionally tighter than green sand molds because they are oven-dried after chemical or clay bonding, trading cycle time and cost for accuracy. Green sand remains the lowest-cost, fastest route for high-volume ferrous castings where coarser tolerance is

Drum ladles dominate heavy-tonnage iron transfer in iron and steel mills, while insulated bucket ladles lose less heat per transfer and suit high-cycle foundry operations. A bucket-style refractory-lined ladle expected to survive 50 to 100 pours per lining cycle is the typical workhorse for mol

Drop bottom furnaces deliver 5-10 second quench delays for thin-gauge aluminum, while roller hearth lines trade that speed for continuous throughput at 5-50 t/h and gentler handling of thin-wall castings. Drop bottom fits 5-100+ ton batch loads needing 5-7 s delays; roller hearth fits continuous sol

Die casting fume extraction systems cut energy use by up to 85% in recirculation mode and remove 1,000+ kg/year of sticky oil-mist per machine, using hood, electrostatic, and demister stages sized to tonnage.

A complete aluminum die casting production cell pairs a 35-500 ton (or larger) cold-chamber machine with a matched breakdown furnace, a robotic extraction/spray unit, a trim press, post-machining, heat-treat, and CMM-based inspection. Specifying tonnage, shot weight, holding-furnace throughput, and

Cylindrical steel ladles lose roughly 5 to 8 percent of bath temperature per hour through the lining and shell, while conical shells trade some additional bottom heat loss for easier solidified skull removal and better teeming flow control.

Cylindrical steel casting ladle refractory working linings typically run 150–225 mm in the barrel and 225–300 mm in the bottom, with a safety lining and insulating layer behind, per IspatGuru. Selection balances heat retention, slag attack and turnaround, and hot-state gunning repair now extends cam

Cupola furnaces and blast furnaces share the same countercurrent shaft principle, but they diverge sharply on charge (scrap/pig iron vs iron ore), product (cast iron vs pig iron/steel feedstock), and slag economics. A process engineer should pick by feedstock availability, target carbon and silicon

Industrial cupola furnace pricing typically spans $200,000 to $2,000,000+ USD, scaling with melting capacity. Small units (1-5 t/h) start around $200,000-$500,000, mid-range (5-30 t/h) cost $500,000-$1,500,000, while large foundry units (30-100 t/h) exceed $1,500,000, with energy and coke cost as pr

A cupola charge layer takes roughly 30 to 60 minutes to descend from the top feed door through the preheating zone into the active melt zone, set by the shaft counter-flow profile, blast rate, and preheating zone height.

Cupola furnaces cannot directly accept coal injection like blast furnaces; coal lowers coke rate only in BF tuyeres. Foundry operators should target 8-12% coke rate, 400-600°C hot blast, and oxygen boosting to cut specific coke consumption.

A cupola's tuyere-to-well temperature profile rises from roughly 1093°C in the preheated charge to about 1600°C in the combustion zone, then drops toward the well where superheated iron collects before tap. Two-row tuyere designs, oxygen enrichment and continuous temperature monitoring shift that pr

Cupola furnace melt rates for cast iron span roughly 1 to 100 tonnes per hour depending on shell diameter, with 450–2000 mm internal diameter units delivering 1–30 t/h and large 13 ft (about 3.96 m) diameter installations reaching 100 t/h. Above 40 t/h, cupola economics dominate over electric meltin

The cupola furnace, a vertical shaft melter using coke as fuel and counter-current heat exchange, remains the historical backbone of cast iron production, with U.S. cupolas still delivering roughly 53% of domestic output and 6.07 million tons per year melted across 23 companies.

Cupola furnace cross section: tuyere belt 0.8–1.4 m above sand bottom supplies combustion air into a well zone that collects melt and slag, with stack, preheat, melting, reducing and combustion zones stacked above.

Mineral wool cupolas burn foundry coke sized around 0.2 m diameter at roughly 13% of the charge to reach about 1,430 °C melt, with oxygen enrichment and hot blast each cutting coke use on a sliding trade-off curve, not eliminating it.

Cupola furnace coke bed height must sit 30 inches (≈760 mm) above the tuyeres to keep the oxidation zone stable; dropping the bed raises top-gas particulates and CO, raising it starves melt rate.

Cupola charge calculation hinges on the iron-to-coke ratio, the limestone-to-coke flux ratio, and the coke carbon content (typically ~85%). Working bands are 6:1 to 10:1 for iron/coke and 10% to 45% limestone on coke, set against tuyere-zone oxidation losses that can reach 65%.

Cupola furnaces transfer carbon from metallurgical coke into molten iron via the dripping bed, with target carbon pickup of 3.2-3.5% C and 2.1-2.4% Si, tuned by coke rate, bed height, and blast conditions.

Cupola furnace capital cost benchmarks land at roughly $225 per annual short ton of installed capacity across the 10-140 tph class, with 2018 industry studies putting capital investment about 25% below a comparably rated medium-frequency induction line. Real plant totals for a 15 tph foundry run $2.

Cupola slag basicity in mineral wool furnaces is governed by the acidity coefficient (Mk), with fiber-formation research pointing to a working window of 1.05-1.20 and a documented 50 °C/s critical cooling rate at Mk 1.05. Iron-foundry cupola practice targets a different index, CaO/SiO2 of 0.5-0.6, a

Silicon carbide crucibles outperform clay graphite in thermal shock resistance, oxidation tolerance, and service life for industrial non-ferrous melting, justifying a roughly 2-3x price premium. Graphite crucibles remain a viable low-cost pick for school shops, intermittent use below 1000°C, and red

Induction crucible furnaces heat the charge directly via eddy currents from a copper coil, while resistance crucible furnaces heat a resistive element that then radiates to the crucible. Direct induction gives faster melt, lower oxidation, and better stirring; resistance designs are simpler, cheaper

Crucible furnaces for small foundries typically span 18 kg to 2,000 kg melt capacity, with 50-200 kg units dominating the small-to-medium industrial segment and fixed units topping out near 1,000 kg.

Coreless induction furnaces deliver higher melting rates (0.5–2 t/h typical in mid-size foundry sizes) and alloy flexibility, while channel furnaces offer 10–15 percentage points higher electrical efficiency for holding the same alloy at temperature. Selection hinges on cold-start vs continuous-hold

Coreless induction furnaces used for aluminium scrap remelt have an intrinsic coil power factor of only 0.1 to 0.3 lagging, corrected to 0.95+ at the grid by integrated capacitor banks and IGBT inverters; energy use sits in the 400 to 550 kWh per tonne range with electrical efficiency above 90 perce

Cold flakes form when a solidified skin grows on the cold-chamber shot sleeve wall and is torn off by the plunger, producing non-bonded polycrystalline inclusions that cut HPDC ductility and UTS.

For aluminum cold chamber die casting, injection pressure typically sits in the 20-70 MPa band, with peak intensification up to roughly 150 MPa, and fast-shot gate velocities of 30-60 m/s. Specification is driven by alloy family, shot weight above 90 g, wall thickness, and clamp tonnage from 135 to

Immediately after amine gassing in PU cold box coremaking, cores reach sufficient basic strength for demolding within seconds, provided gassing pressure stays in 2-30 PSI and amine vapor fully saturates the sand. Residual amine past the wash step degrades moisture resistance and lengthens bench life

Hot box core shooters cure resin-coated sand at 250-350°C core box temperatures with 40-120 s shell hardening, giving higher dimensional accuracy but longer cycle times. Cold box core shooters cure at room temperature using triethylamine gas, delivering short cycle times and higher production effici

PU cold box core shooting typically operates at 2.5–6 bar blow pressure with shot chamber capacities of 12–60 L on commercial machines, while small jobbing units run 10–20 kg cores at 5–7 bar and high-tonnage cells scale above 30 kg per cycle.

Optimum cold box core shooting runs 2.5-4.0 bar blow pressure at short fill times, with fill pressure rising toward 5 bar for dense section cores. Sand compaction, amine cure uniformity, and blow-hole rejection all track those two parameters first.

PU cold box core making is a two-stage process: sand-resin shooting, then amine gassing followed by a compressed-air purge to harden the core and clear residual catalyst. Fill density, gas pressure, and purge duration each shift core strength, amine carry-over, and vent line condition on cold box co

Cokeless cupola furnaces replace coke with natural gas burners firing through a bed of refractory ceramic spheres, with reported fuel use of 50–55 m³ natural gas per tonne of iron and sphere consumption of 1–1.5%.

CO2-cured alkaline phenolic cold box binders run at 1.5–3.0% resin on sand weight with no amine or methyl formate exposure, while amine PUCB remains the higher-strength default for high-volume cores. Pick CO2-phenolic when VOC/odor and amine scrubbing capex matter; pick amine PUCB when bench life, t

Channel (core-type) and coreless induction furnaces are not interchangeable: choose the channel design for high-volume holding and lower-melting-point non-ferrous alloys, and the coreless design for cold-start melting, alloy flexibility, and difficult metals like cast iron and stainless steel.

A channel-type induction furnace cannot be drained cold; it requires a permanent molten heel in the channel loop to complete the secondary circuit and carry induced current, which is why these units are dedicated to one alloy and avoid heel swaps.

For a cupola blast-air duty at 15-25 oz/in² (≈6.4-10.8 kPa) and multi-thousand CFM, positive-displacement rotary lobe blowers remain the default blast supply on North American iron cupolas, while centrifugal units take over above ~15 PSIG discharge or where air density and tuyerere pressure drop mus

Cement-bonded briquettes solve a long-standing problem in the rock wool cupola: they let fine mineral wool waste and stone dust re-enter the melt at controlled, predictable feed rates. Calcium-aluminate or Portland cement binder at 10-15% by mass is the standard, with rockwool content up to 50% of t

Die casting mold cost is driven primarily by cavity count, slide/side-action count, and tool steel grade, with multi-cavity large aluminum dies typically ranging 80,000 to 250,000 USD. Each major driver can shift tooling price by 10 to 50 percent, so engineers should compare total landed cost across

The ladle is the last vessel that touches liquid metal before pouring, and it is where temperature trim, alloy trim, slag separation, and preheat discipline converge to determine casting soundness. Bottom pour, lip pour, and teapot configurations differ in capacity, stopper preheat, and slag control

Ladle slide gate plates use alumina-carbon, alumina-zirconia-carbon, magnesia-carbon, or zirconia refractories to throttle molten steel flow from 20-350+ ton ladles, with FF two-plate linear designs now extending plate life past conventional Flocon systems.

An investment casting foundry's equipment list spans seven process stages: wax injection, ceramic shell building, dewaxing furnaces, metal-melting furnaces, pouring, shakeout, and finishing. Core capital items include aluminum wax dies, slurry tanks and stucco fluidized beds, steam autoclaves or fla

A complete aluminum high-pressure die casting cell pairs a cold-chamber HPDC press rated 250-1600 tons with a holding furnace, melt transfer system, die lubrication/extraction robots, trim press, and downstream heat treat, blast, CMM, and CNC finishing. Most US shops run 380-series alloys; a single

A complete sand casting foundry line combines melting, sand preparation, molding, core making, pouring, shakeout, finishing, heat treatment, and QA stations; the equipment list below maps each station to capacity and function based on a documented 5 T/h iron foundry configuration.

Yes, squeeze casting of wrought 6061 aluminum is technically validated: applied pressure of 60-90 MPa cuts porosity and refines dendrites, yielding as-cast or T6 mechanical properties comparable to wrought 6061 stock. Process trade-offs include Mg2Si segregation at thick sections, narrow 60-80 MPa p

Cupola iron cannot be used directly for ductile iron without desulfurization: the coke bed drives sulfur pick-up well above the 0.015-0.020% ceiling that magnesium treatment requires, so in-stream or ladle desulfurization is mandatory before nodulizing.

Yes, a gas-fired crucible furnace can reach cast iron melting temperatures, provided it is built for the duty: cast iron melts above ~1147°C at roughly 4.3% carbon, and a refractory-lined gas furnace with a clay-graphite or silicon carbide crucible can sustain the 1200-1400°C chamber range required.

A standard coke-fired cupola cannot hold molten carbon steel above 1536°C while keeping carbon low; charging low-carbon steel scrap causes it to absorb carbon from coke and exit as cast iron, not as carbon steel.

Calcium cored wire injection modifies solid Al2O3 inclusions into liquid calcium aluminates at recoveries of 25-55%, versus 5-15% for bulk CaSi, with pure-Ca wire (97% Ca) the top performer on yield and cost.

Brass and aluminum squeeze casting machines differ mainly in melt temperature, die material and clamp-force demand. Aluminum units lead the market for automotive structural parts, while brass machines stay the choice for bushing and gear foundries running copper alloys above 900 deg C.

Brass squeeze casting machines for small valve bodies typically run 8-25 shots per hour per cavity, with cycle time dominated by 5-10 min of pressure-hold solidification rather than injection; output is set by tonnage, melt temp, and pour weight, not machine speed.

Brass squeeze casting fills the gap between high-pressure die casting and forging for plumbing fittings, delivering near-zero porosity, tensile strength above 300 MPa, and complex near-net-shape geometry on standard plumbing components.

Bale-out crucible furnaces at aluminum die casting cells melt in a refractory-lined crucible and are dipped by hand-held ladles, sidestepping pressurised launder systems. Typical sizes run 100-500 kg Al per batch, with electric-resistance or gas-fired top heat.

Amine catalyst dosing in cold box core making targets 0.3–0.5% initial DMEA or TEA concentration with 0.15–2 bar gassing pressure, curing cores to 99% hardness in seconds at room temperature. The binder system is a two-component polyurethane (phenolic resin + MDI, ~70% of the formula) gassed with te

Aluminum squeeze casting machine pressure range of 20 to 30 MPa, maintained for 5 to 10 minutes through full solidification, is the working window for near-zero porosity aluminum parts per peer-reviewed process literature. Machines below 50 MPa clamp force behave as ordinary die casters and will not

Aluminum induction holding furnaces operate between 680 and 750 °C, with pure aluminum melting at 660 °C and alloys typically controlled at 700–750 °C for stable fluidity. Above 750 °C, refractory attack and oxidation losses rise sharply, so most specifications target 720 ± 20 °C.

For thin-wall aluminum HPDC parts, machine tonnage is sized by projected area and specific pressure: typical safety factor 1.0-1.3 (1.3 for thin/complex geometry), with commercial cold-chamber machines spanning 135-3500 metric tons, so 250-1600 ton cells dominate structural thin-wall work.

Aluminum HPDC dies built from H13 tool steel (AISI H13 / DIN 1.2344 / JIS SKD61) routinely fail by die soldering, a metallurgical bond driven by Fe-Al intermetallic phases such as η-Fe2Al5. Operating hardness of 42-48 HRC, surface treatments (nitriding + PVD CrN/TiAlN), and release-agent chemistry a

For A380 and ADC12 (effectively the same Al-Si-Cu chemistry, different naming regions), cold-chamber die casting injection pressure sits in a 60-120 MPa intensification range, with A380 favoring 70-90 MPa on large thin-wall automotive shells and ADC12 commonly specified at 80-90 MPa on electronics e

Aluminum die casting productivity hinges on matching water-miscible release agent chemistry to alloy silicon content (commonly 7–13% in A380/ADC12/A360/A413) and shot fluidity, with die temperature, dilution ratio, and spray pattern controlling fill and surface finish.

AlSi10MnMg suits structural and corrosion-sensitive EV die castings with 0.05% max Cu and up to 0.8% Mn, while AlSi9Cu3(Fe) fits thin-wall high-volume HPDC parts needing 2.0–4.0% Cu for machinability. Charpy impact tests show AlSi10MnMg absorbs 1.5–3.7x more energy than ADC12, making it the better p

Alkaline phenolic (no-bake) sands are best reclaimed by thermal calcination above the resin decomposition threshold, because mechanical attrition leaves potassium and sodium salts that shorten bench life and impair strength. Thermal reclamation is the only path that fully strips cured alkaline resol

A356-T6 squeeze castings deliver typical tensile strength of 290-310 MPa with 8-12% elongation, outperforming gravity permanent mold (262 MPa / 5%) and sand (234 MPa) castings of the same alloy. Source ranges from peer data and ASM handbooks put T6 UTS between 200-310 MPa, with yield at 165-230 MPa

For prototype injection runs under ~50,000 shots, 7075 aluminum cuts lead time to 2–5 weeks and cycle time by ~30% versus P20 pre-hardened steel; above 50,000 shots or with glass-filled resin, P20's 100,000+ shot life wins on total cost-per-part.

For a single casting or a small batch under ~10 pieces, binder-jetted 3D sand molds beat patterned green-sand molds on geometry, lead time and fettling, at roughly $120 per mold versus $15 per use amortized. Above that batch size, conventional patterns win on unit cost, so the break-even sits in the

A 2000 ton cold chamber die casting machine weighs roughly 120-180 tonnes fully rigged, so a single 100/80 tonne overhead crane pair is too small; the lift typically needs two 100 tonne cranes in tandem, a single 200+ tonne crane, or a heavy-duty gantry. Crane capacity, rigging, and foundation desig

A 2000-ton class cold chamber die casting machine typically delivers 19.4 to 30.3 kg net shot weight of aluminum, with clamping force around 2000 ton, tie-bar spacing near 1350×1350 mm, and casting pressure 622–1237 kgf/cm² depending on plunger diameter.

For large mold base plates above 400 mm thickness, DIN 1.2738 (P20+Ni) is the correct specification over standard P20/1.2311: the nickel-bearing grade delivers higher through-thickness hardness uniformity, longer service life, and is qualified for hot-work mold base frames, while 1.2311 is the cost-

1.1730 (DIN C45W, ~640 MPa) is the cheap, unmachinable-hardenable frame/backing plate steel; 1.2311 (P20, ~1050 MPa, 28-32 HRC) is the pre-hardened all-rounder for mold bases; 1.2312 (P20+S, ~1050 MPa) adds ~0.07% sulfur for free-machining, used for stress-bearing plates. Pick by hardness, polish, a

Shell molding machines for telecom enclosures typically run Croning tool temperatures of 250-350°C, with platens from 15×20″ up to 30×44″ and core box depths of 7.5-20″, suiting iron castings rather than thin-wall aluminum covers. For EMI/RF housings under 3.2 mm wall thickness, high pressure die ca

Vacuum die casting evacuates the die cavity to under 100 mbar (often below 60 mbar in high-vacuum variants) before molten metal injection, eliminating gas porosity so parts become weldable and T6-heat-treatable, at the cost of tighter process control and sealed tooling.

Cold chamber die casting machine failures concentrate in four modes: thermal fatigue at the injection sleeve and plunger tip, gas porosity and oxide inclusions during metal transfer, soldering and heat checks on the die surface, and hydraulic injection system drift. A spec-anchored prevention progra

Cold chamber die casting machine spare parts and consumables span shot sleeves, plungers, injection heads, ejector pins, hydraulic valves, and die lubricants, sized to 90+ gram shot weights and 10,000+ psi injection. Selection follows a wear-zone and shot-weight logic, with hot-chamber overlap only

A cold chamber die casting machine inspection covers eight systems: die condition, shot, clamping, ejection, temperature, lubrication, cooling, and casting quality, with clamping force calculated as cavity pressure × projected area. For aluminum and magnesium work targeting shot weights above 90 g,

Selecting an induction furnace for telecom-enclosure fabrication hinges on matching mains- or medium-frequency power, copper-coil current density, and 625 kWh/ton steel-melt energy to aluminum or stainless output. Capacity spans from sub-kilogram tabletop units to 100 t mains-frequency coreless furn

A cold chamber die casting machine typically runs 15-25 years with disciplined maintenance, but high-cycle aluminum foundries often face replacement decisions at 8-12 years on the shot end, hydraulics, and tie bars. Trigger-based overhaul beats calendar-based replacement: target the closing unit, hy

Electronics-housing static pressure molding lines run reliably when hydraulic oil sits at 30-50 degrees C, heater bands are audited quarterly, and ejector pins are checked straightness-wise every shift. Skip those, and a 150-ton press will burn $12,000-$28,000 per unplanned 8-hour stop.

A cold chamber die casting machine injects externally melted aluminum (or other high-melting-point alloy) into a steel die at 7-350 MPa via a hydraulic plunger, keeping the shot sleeve, gooseneck, and melt pot physically separate to avoid iron pickup and thermal damage. This separation, plus cycle-c

H13 shot sleeves in cold-chamber die casting fail mainly from thermal fatigue, gross cracking, pour-hole washout, and piston-to-bore clearance growth; prevention hinges on heavy walls, Rc 46-48 hardness, gas nitriding, and bore-weld repair with W.Nr. 1.2367.

A molding line combines five core stages, plastification, injection or fill, compaction, demolding, and finishing, into one continuous flow, with the dominant process dictated by material state: thermoplastic melt for injection, parison inflation for blow, or sand compaction for foundry molds. The t

Shot sleeve spare parts fall into four consumable groups: blast wheel blades, control cages and directional sleeves, impellers/distributor wheels, and chamber liners; matched by machine model, photos, and key dimensions. Common materials include high-chromium alloy, manganese steel, and hardened cas

Cupola furnace failure modes cluster around refractory lining attack, tuyere and shell erosion, crucible reaction in duplex melting, and emissions-side thermal stress. Prevention hinges on TPK efficiency control, hot-blast recuperation at 400-600°C, and tight C/Si melt chemistry, with MACT-compliant

Crucible furnace TCO over a 10–15 year service life is driven by crucible replacement, energy (kWh per kg of melt), refractory maintenance, and labor, not by the headline purchase price. Lifecycle cost typically runs 3–6x the initial capital outlay once consumables, power, and downtime are loaded.
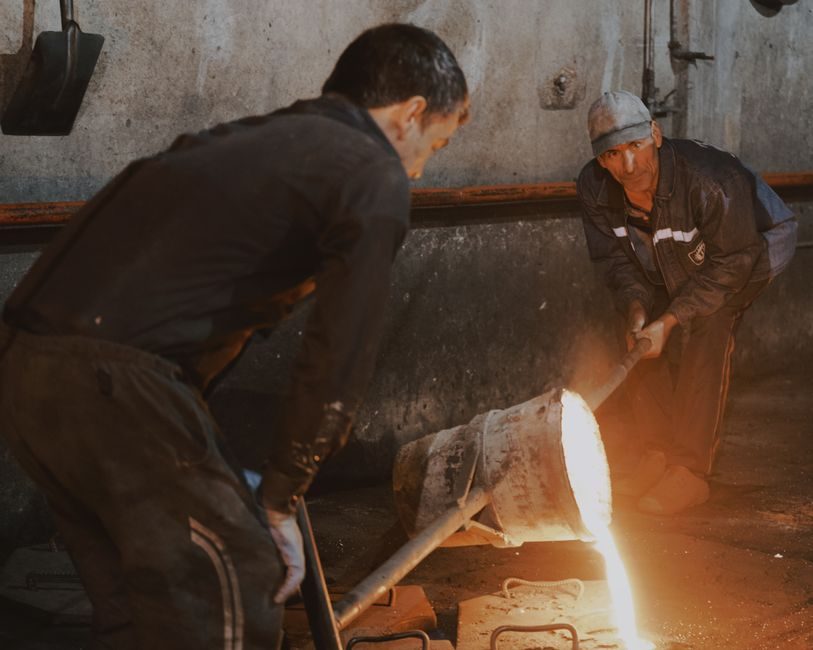
Casting ladle total cost of ownership spans purchase, refractory relines, energy, ladle preheating, and lost steel — refractories and downtime dominate 5–10 year spend. Steel-plant buyers who model five cost lines, not sticker price, control 60–75% of lifetime cost.

Chinese aluminum extrusion profile suppliers listed 2026-07-29 cluster around AA6063-T5 and AA6061-T6 alloys, 5-ton MOQs, US$2,800-2,900/ton FOB price bands, and GB 5237 surface finish classes for construction, doors, and windows.

Melting furnace selection for automotive parts hinges on alloy, melt rate, and energy source: induction dominates steel and vacuum-grade alloys, gas/crucible furnaces suit aluminum, and holding furnaces stabilize tap temperature before die casting.

For aerospace component production, choose a crucible furnace that matches alloy chemistry, AMS2750 thermal-uniformity class, and atmosphere control, with induction, vacuum arc, and resistance-heated cold-crucible as the three primary options.

Gravity die casting machines install on a prepared reinforced foundation with a 30-40 ton/month-class aluminum output envelope, tilt-pour or fixed-pour configuration, and tied-in molten-metal safety per foundry EHS practice. This guide covers site prep, rigging, alignment, commissioning and acceptan

For telecom enclosures, a shell molding machine sized to 800×600 mm flasks with phenolic resin and 200-280 °C plate temperatures fits 5G radio housings; plastic molding dominates indoors, die-cast aluminum leads outdoor IP67 builds, per 2026 supplier data.

Investment casting equipment selection hinges on four matched decisions: alloy family, shell-building process (water-glass, silica sol, or lost-foam), wax/dip line capacity, and post-cast finishing throughput. Specifying all four against part geometry, annual tonnage, and surface tolerance avoids th

Low-pressure die casting machines (LPDC) pressurise molten metal from 0.1–1.0 bar to feed a die from below, suiting aluminium wheels, engine blocks and structural parts where gravity die casting leaves porosity.

Railway brake shoes, bolster covers and pantograph bases are cast in iron or steel, so the bottleneck is the automatic molding line: 60-180 molds/hr horizontal flaskless units with 500-1200 mm flask sizes and 8-12 kgf/cm2 squeeze pressure dominate 2026 deliveries, while static-pressure green-sand li
Hot chamber die casting machines in the 16-180 ton clamping range suit zinc and Zamak lighting fixture housings under 1 kg shot weight. Selection pivots on locking force, plunger diameter, shot weight, die height, and a real-shot test rather than catalog tonnage. Lighting buyers must reject hot cham

For telecom enclosures, an aluminum die casting machine is typically specified in the 400–850 ton cold-chamber HPDC range, paired with real-time shot monitoring and robotic extraction to meet IP-rated housing tolerances.

Specifying a holding furnace for agriculture-machinery casting starts with alloy and tonnage: 1-3 t/h grey-iron or ductile-iron flows pair with channel or coreless induction holding units, while higher-tonnage steel casting or continuous casting lines move to gas-fired reverberatory holding or cruci

Molding lines deliver cycle times of 10-60 seconds and per-part costs that collapse at volumes above 10,000 units, but the trade-off is heavy: mold tooling capital, design-lock-in, and clamp-force limits that rule out large hydraulic parts. Electric, hydraulic, and toggle presses each carve a differ

Magnesium die casting suits thin-wall, weight-critical parts under ~5 kg where steel and aluminum are too heavy; choose hot-chamber for sub-1.5 mm walls and high volume, cold-chamber for larger structural castings, and verify alloy, machine tonnage, and protective atmosphere before sourcing.

Cupola furnaces are a poor fit for electronics housings: their iron-rich, high-carbon melt (Fe reduction 50–70% in pilot Mn-ore work) and coke-driven 1400–1500 °C operation cannot deliver the tight C, Si, P, and inclusion control that aluminum die-cast and zinc/zamak housings demand. Specify in

Cast steel and iron ladle assemblies for agriculture machinery are dominated by Chinese foundries offering low-alloy, high wear-resistant grades in the US$0.60–200.00 unit range, with MOQ 100 pieces and 10,000 t/yr capacity. Selection hinges on part geometry, alloy family, and required batch size.

Pick a hydraulic press by matching tonnage, frame style, and drive type to the workpiece: H-frame for heavy/straight-side work, C-frame for off-center access, 4-post for symmetrical forming, and servo-hydraulic for 30-50% energy savings on variable-load cycles.

For lighting fixtures, mold the LED aluminum channel/heat-sink housing and the polycarbonate lens with a precision molding line, not a decorative interior crown profile. Specs that matter: profile tolerance ±0.1 mm, aluminum 6063-T5 for thermal conductivity ~209 W/m·K, IP65 optical-grade PC lens, an

Cold chamber die casting machines are specified in the 200-5000+ tonne locking-force range for aluminum, magnesium and brass alloys; sizing must align shot weight, projected area and tonnage to avoid flash or die sticking.
Spec a gravity die casting machine by clamping force 50–800 kN, platen size 400×400 to 900×900 mm, melt capacity 5–150 kg Al or 30–300 kg Cu/Zn, PLC+touchscreen, and matched die-set steel. Brass faucets, aluminium valve bodies, and low-volume structural castings fit; thin-wall consumer electronics d

Hot chamber die casting machines are generally unsuitable for aerospace structural parts because their alloy envelope is limited to zinc, magnesium, and lead-family low-melting alloys. Aerospace buyers should instead specify cold chamber or vacuum die casting for aluminum and magnesium airframe comp
Hydraulic presses convert fluid pressure into linear forming force, with tonnage, frame architecture, and duty cycle governing selection. The PBM 100 M shop press delivers 100 tf at 350 bar with a 500 mm stroke, while Chinese vulcanizing presses span 20–5,000 tons across H, C, four-pillar, and frame

Verified 2026-07-07: induction-melting lead times on Made-in-China cluster 30-60 days for 500 kg-5 t units, FOB Ningbo/Luoyang; gas crucible and holding furnace lines dominate aluminum scrap and SiO2 glass.

Cold chamber die casting machines in the 800-900 ton clamping range with shot weights of 8-12 kg aluminum are the practical baseline for rail components, matched to EN 1706 / EN 13261-style alloy specs and 60-110 MPa intensification pressure.
Hot chamber die casting machines in the 16-180 ton clamping range cover 90% of zinc and zinc-alloy electronics housing work. Selection hinges on shot weight, platen size, and injection velocity for thin-wall connector shells.
A zinc die casting machine priced at $10,000-$22,000 new delivers its lowest 10-year cost when sized in the 25-90 ton hot-chamber band; below that, tooling and yield losses dominate, above it, energy and idle capacity eat the savings.
Die-cast shot-sleeve TCO is dominated by downtime, lube, water and rework, not the sleeve price; buyers who line-item those four buckets typically cut 5-year spend 18-28% versus per-piece purchasing.
Casting molds trade tooling rigidity for part geometry: permanent/sand/die casting molds deliver near-net shape, complex cavities, and low per-part cost above break-even runs, while cycle time, size limits, and alloy restriction define the boundaries. Pick on geometry, volume, alloy, and surface spe

Gas-fired aluminum melting furnaces are sized by holding capacity (typically 1-50 t per station), specific energy consumption (550-700 kWh/t or 40-55 Nm³ NG/t at 900-760 °C melt) and burner thermal output (≈1.2-1.5 MW/t). Selection pivots on melt rate, alloy family, refractory lining and flue-gas he

Gas-fired aluminum melting furnaces in the 5-10 tonne capacity class remain the dominant specification for automotive parts foundries, with 2026-vintage OEM models from Guangdong, China offering combined melting-and-holding designs at 4 sets/month production cadence, targeting A356/6061 alloy throug
High-pressure die casting injects molten metal at up to 150,000 kPa (21,700 psi), producing thin-walled, complex parts in seconds — but only when production volume justifies tooling cost. Die casting dies pair a die casting machine with a hardened steel mould rated for thousands of cycles, and the t

Rail component die casting centres on 1000-2500 t cold-chamber machines, with hot-chamber zinc units reserved for sub-1 kg interior brackets. Material, tonnage, and shot-weight alignment govern machine class selection.
Sand mixers deliver uniform bentonite/water/aggregate blending in 3–8 min cycles, but trade shaft-seal wear, energy draw, and cleanup time against throughput. This map lines up continuous vs. batch, wheel vs. vertical, and resin vs. green-sand duty so buyers can pick on cycle time, m³/h, and binder
Installing a cupola furnace requires a reinforced foundation, refractory lining, controlled cold/hot blast, and pollution control gear sized to melt rate; P.S Trading Co. lists cupola, ladles, and dust collection as one integrated scope.
Magnesium die casting machine selection hinges on five spec levers: clamping force (kN), hot-chamber vs cold-chamber architecture, shot weight (g), Mg-specific melt handling, and IATF 16949 / ISO 9001 build quality for automotive programs.
Low pressure die casting (LPDC) machines fill the gap between gravity casting and high-pressure die casting: fill pressures typically 1-4 bar, holding pressures 20-100 kN on the shot cylinder, and locking forces rarely above 100 t. Selection gates are alloy, shot weight, platen envelope, cycle time
Agricultural machinery foundries specify furnace class by alloy, melt mass, and batch rhythm: cast iron cupola or induction furnace for 500–5000 kg batches, crucible furnace for low-volume alloy swaps, holding furnace for pour-line buffering.

Spec a shell molding machine around shot weight 5-50 kg, platen size 600x500 to 1200x1000 mm, and 0.4-0.6 MPa curing air, matching a shell molding line cycle of 30-90 s.

China-origin V-process vacuum molding lines ship in a 1-3 month peak / 3-6 month off-season band from Shandong and Jiangsu OEMs, with Qingdao Shengmei as a named cluster reference.

Gas-fired aluminum melting furnaces for electronics housings require clean-combustion burners, low-Mg alloy handling, and refractory choices that protect die-cast surface finish. Selection pivots on melt rate, dross loss, and atmosphere control, not just BTU input.
Hot chamber die casting machines are specified for zinc, magnesium, and lead alloy hardware runs where cycle time under 1 second and tonnage between 16 and 180 t matter most. Selection pivots on locking force, shot weight, platen size, and gooseneck metallurgy rather than brand. This map lines up th

Shell molding machines are classified into three principal types — manual, semi-automatic, and fully automatic — by drive mode, clamping force, and shot weight, with the shell molding machine category spanning compact bench units under 50 kN clamp to 1,000+ kN integrated molding line cells producing

Line frequency induction furnaces (50/60 Hz mains-frequency coreless or channel units) remain the workhorse for iron, steel, and large-tonnage hardware foundries, but selection hinges on batch size, melt rate, scrap preheating, and power-supply stability rather than kW rating alone. Hardware plants
Hot-chamber die casting machines below 160 tonnage dominate zinc-alloy production in 2026, with SH-25-class units and 23-machine job shops leading North American supply. Sourcing levers: tonnage, platen, shot weight, and hot-chamber build.
Vacuum die casting machines for energy equipment are specified by clamping force (kN), vacuum level (mbar), alloy family, and shot speed. Selection differs sharply from standard die casting because gas porosity in transformer housings, switchgear, and busbar enclosures is a dielectric failure mode,
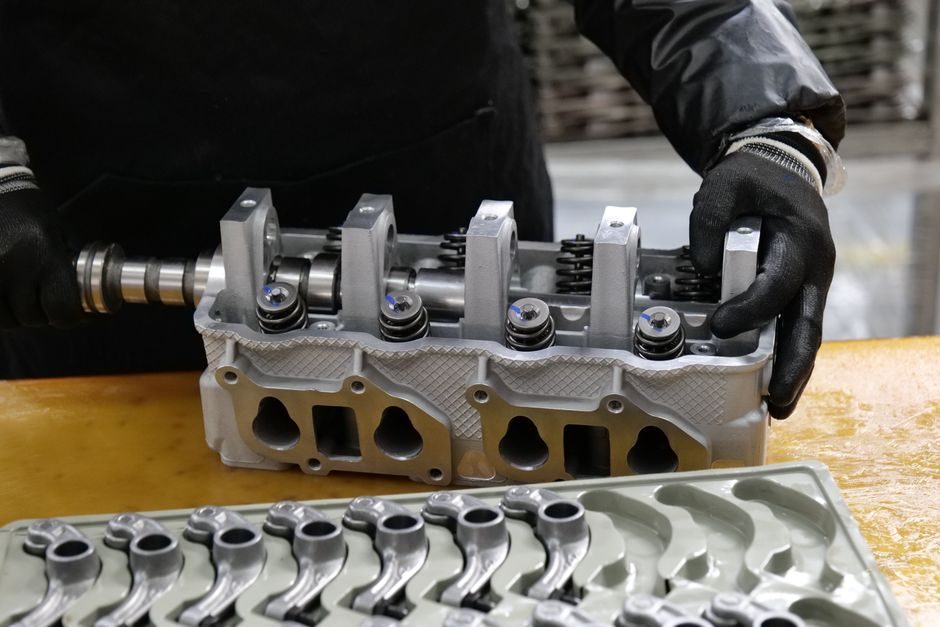
For safety-critical automotive aluminium parts (knuckles, control arms, suspension links, pump housings), squeeze casting delivers near-forging density at HPDC-toleranced geometry, and the practical selection gate in 2026 is a direct vs indirect process match, a clamping-tonnage envelope of roughly
Squeeze casting and hot chamber die casting are not interchangeable: squeeze casting applies slow, high-pressure solidification to aluminum and brass structural parts (HYBERS, CENS, 2026-04), while hot chamber machines cycle zinc and magnesium alloys at production speeds (HYBERS lists 16–180 ton hot
Cupola furnace selection hinges on melt rate, charge mix, metallurgical coke quality, lining life, and emissions control. Match diameter, tuyere count, hot-blast ratio, and shell height to iron grade and daily tonnage before specifying equipment.
Hot chamber die casting is a zinc- and magnesium-alloy process unsuited to most aerospace structural parts; cold chamber machines dominate the aerospace aluminum/magnesium segment, and buyers commonly misread the two technologies. This article sorts the process boundaries, machine-spec levers, and t
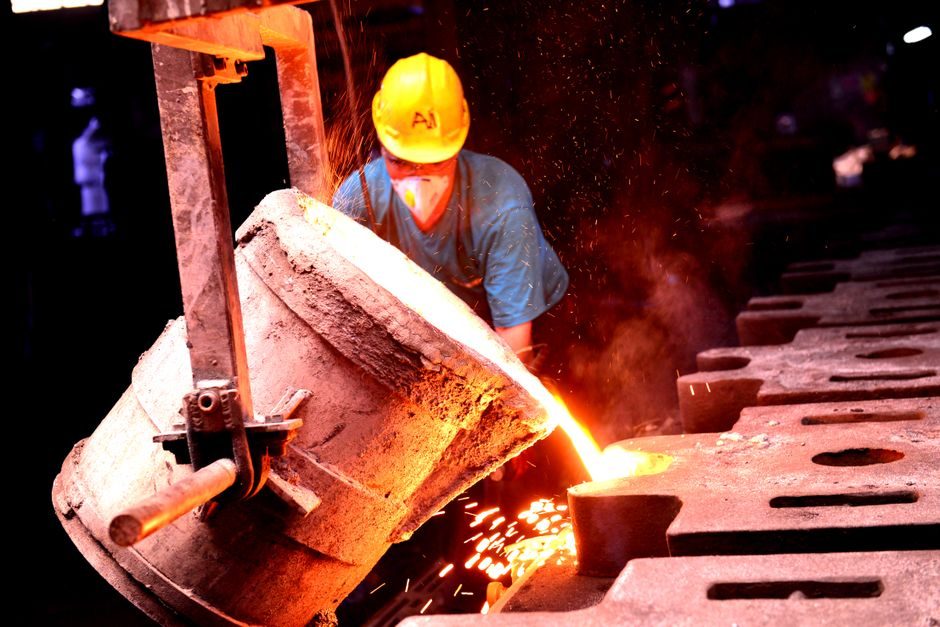
Channel/coreless induction furnaces deliver 1,200-1,800°C clean, controllable melt with >60% electrical efficiency, but require cooling water, power-factor correction, and careful refractory selection to remain cost-competitive against gas-fired melting furnaces.

Magnesium die casting machine selection hinges on tonnage class, hot-chamber vs cold-chamber architecture, and locking force matched to projected area. Most OEM cells in 2026 cluster between 300 and 9000 kN, with hot-chamber dominating sub-1000 kN magnesium work.

Static pressure molding machines for green-sand foundry lines are selected by flask size, squeezing pressure (typically 0.5-1.5 MPa specific pressure), sand throughput and cycle time; matched to molding line throughput and shot weight.

Line frequency induction furnaces operate directly off mains 50/60 Hz without static frequency converters, suiting 1-40 t aluminum melting for telecom-enclosure casting at 8,800-180,000 USD per set on 2026-07 listings.
Chinese investment-casting suppliers continue to dominate global sourcing, with 2,000+ manufacturers on Made-in-China.com and precision lost-wax part prices from US$0.10-0.45/piece as of July 2026. Buyers should benchmark on ISO 9001:2015 certification, material capability, and verified audited-supp

Magnesium cold chamber die casting machines with 800-1600 t clamping force and SF6/N2 gas-protected melting-dosing units are the dominant configuration for agricultural machinery housings, bracketry, and gearbox shells in 2026. The recommended selection path matches clamping tonnage, shot weight, an

Die casting machines deliver high-volume, near-net-shape production of complex non-ferrous parts at cycle times as short as 8 seconds, with cold-chamber lockup forces spanning 300–3500 t, but they demand high capex, die wear management and energy input that limit them to long-run work.

Aluminum coils are rolled sheet stock for fabrication; aluminum die casting machines (cold chamber 80T–900T, $10k–$80k) shape molten Al/Zn alloys. Buyers needing flat stock for stamping should source coils; those needing net-shape parts should specify die casting tonnage and alloy.
Foundry sand mixers are selected on five engineering criteria: batch capacity (kg/cycle), impeller tip speed (m/s), muller wheel loading (kg/kW), bowl lining material (Ni-Hard / SS / polyurethane), and a PLC recipe-handling level matching the binder system (furan, phenolic-urethane, green bentonite,
Zamak 3 and Zamak 5 cold-chamber zinc die casting machines in the 80-160 ton clamping range are the default spec for telecom enclosures under 1.5 kg, with shot weight sized to the part + 30% pad and injection pressure held above 30 MPa for RF-tight wall integrity.
Lost foam casting line selection hinges on foam density (typically 0.015-0.025 g/cm³ for EPS), refractory coating rheology, vacuum holding capacity, and throughput-matched sand handling — a complete lost foam casting line replaces bonded sand shakeout in low-carbon steel and ductile iron work.

Hot box core shooters fit electronics-housing cores in the 0.5-10 kg range when wall thickness stays above 8 mm, draft at 1.5° minimum, and annual volume falls between 5,000 and 200,000 cores. For sub-0.5 kg thin-wall connector shells, a shell core machine typically wins on finish and cycle time.

Die-cast aluminum (ADC12 / A380) and magnesium (AZ91D) dominate electronics housing builds, paired with cold-chamber die casting on 160T to 1200T presses and ±0.01 mm post-machining tolerance for thin-wall, thermally conductive enclosures.

Low-pressure die casting (LPDC) machines are the right call for energy equipment when the part is a large, complex aluminum or magnesium housing that must be near-net-shape with low porosity. For wind-turbine hubs, motor housings, and EV battery enclosures, specify clamping force, crucible and mold

Hydraulic press FOB prices in mid-2026 span roughly US$10,000 for a 200-ton 4-column servo press to US$100,000-800,000 for 3,000-8,000 ton forging wire-winding machines, with tonnage, frame style and PLC/automation tier driving 80x cost spread.
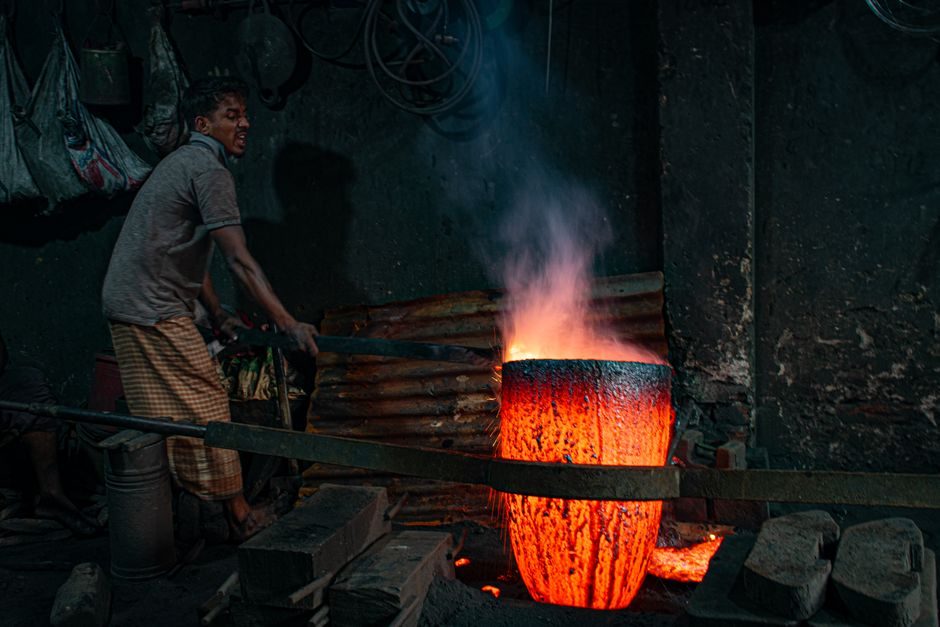
Pick a melting furnace by matching alloy chemistry, charge weight and melt rate to one of four main types: induction, gas-fired crucible, cupola or holding furnace. Wrong pairing wastes 30-50% of energy, which the research ties directly to smelting as the foundry's largest cost line.
Hot-chamber magnesium die casting is the dominant process for rail interior and seat structural components, with selection driven by clamping force (typically 1600-9000 kN), shot weight, and creep-resistant alloy choice above 120°C. Use this guide to match a magnesium die casting machine to EN 45545

For lighting fixtures, squeeze casting suits aluminum heat-sink housings 3-5 mm thick requiring low porosity; for thin-wall decorative parts, HPDC on a cold-chamber machine remains faster and cheaper.

A 10-year TCO for a Lost Foam Casting Line ranges from roughly $2M to $15M+, with EPS pattern tooling at 8-15% of capex, energy 12-20%, and unbonded sand reclamation dominating variable cost. This guide ranks the cost drivers, quotes a comparison against green-sand and automatic molding line alterna
Squeeze casting machines for aerospace components should be selected around 250-ton hydraulic press capacity, sustained pressure during full solidification, and NADCA 2015 spec compliance for aluminum-alloy structural parts. Heavy-load turbine blades, domes and brake-valve bodies are the primary tar
An automatic molding line integrates flask handling, sand delivery, compaction and de-flasking in one continuous cycle, while a core making machine is a single-process station that produces sand cores only. The two are complementary on most foundries, not substitutes: pick a line when you need 80-20
Magnesium die casting (AZ91D, AM60B) at 1.8 g/cm³ delivers 30% weight saving over aluminum for thin-wall EV and 3C parts; choose hot-chamber for under ~1 kg shot weight and cold-chamber above it, with 400–5000 t clamp force matched to projected area.

Foundry Degassing Units (FDU) for automotive aluminium castings target a Density Index of 3-4% and a refining-cycle temperature drop of 26-32°C, with hydrogen removal efficiency and cycle time as the primary selection drivers.
Cupola furnaces remain in service for rail-component iron foundries that need continuous, high-tonnage, low-capex melting, but induction furnaces are the dominant retrofit when foundries need tighter nucleation control, lower emissions, and synthetic metallurgy. Buyers should pick cupola only when c

A die-casting shot sleeve inspection checklist pairs visual checks (scoring, erosion, cracks, metal buildup) with quantitative measurements (inner diameter, ovality, straightness, wall thickness). Standard sleeves span inner diameter 80–150 mm, length 400–1400 mm; sleeves passing all checks typicall

Cold-chamber die casting shot sleeves typically fail at the pour-hole bore and survive 20,000-30,000 shots per inner liner; reconditioning, bore welding with W. Nr. 1.2367, or thermoregulated envelope designs can restore life and cut sleeve cost up to 60% over five replacements.

V-Process (vacuum sealed) molding lines deliver binder-free dry sand molds at 3-7 molds/hr, holding ±0.2-0.5 mm/25 mm tolerance and Ra 6.3-12.5 µm as-cast finish under 50-100 kPa vacuum, making the process a fit for electronics housing castings where dimensional accuracy and clean emissions matter.

A rubber insulating sleeve fails the dielectric test when a 1-minute AC proof voltage per ASTM D1051 / F496 (Class 00 through Class 4) causes breakdown, visible arcing, or leakage above the lab's rejection threshold, and OSHA 1910.137 mandates re-test every 12 months before first issue and after rep

A shot sleeve is the cold-chamber cylinder that holds molten aluminum (or brass) ahead of a horizontal plunger and feeds it under high pressure into a die cavity. The component operates between roughly 320 °C and 680 °C inner-wall temperature, with hot-end-to-cold-end differentials of 100-150 °C dri
Hot chamber die casting machine failures fall into three clusters: hydraulic/power (oil pump, thermal relay, proportional pressure valve), defect-driven (heat checks, soldering, porosity, flash), and mechanical wear (plunger, gooseneck, die surface). Prevention is dominated by cooling-line disciplin

Hot chamber die casting machine spare parts and consumables include goosenecks, plungers, sleeves, nozzles, dies, and release agents, with replacement cycles driven by zinc and magnesium alloy service temperatures and shot counts. Specifying the right consumable grade cuts unplanned downtime and pro

Hot chamber die casting machines built on Zamak and magnesium programs routinely deliver 10–20 year service lives when OEMs follow prescribed preventive maintenance, with replacement decisions driven by shot count, pl

Hot chamber die casting machine commissioning follows a staged sequence: dry-run checks, hydraulic and clamping force verification on a zinc or magnesium alloy load, gooseneck/nozzle preheat, shot-weight calibration, and signed-off first-article inspection before production release. Expect a 0.7-2.8

Hot chamber die casting injects low-melting-point alloys (zinc, magnesium, lead-based) from an integrated melting pot through a gooseneck into a steel die at high pressure, achieving cycle rates up to 10 per minute. It suits small, thin-walled, high-volume parts under roughly 1 kg, and is not used f

Die casting machine failures split into two layers: hydraulic-electrical faults (oil pump no-start, thermal relay trip, no total pressure) and die/tool failure modes (heat checking, soldering, erosion, corrosion, gross fracture). Prevention hinges on coupling clearance of 3-5 mm, AISI H13 hot-work t

Static-pressure molding lines for energy-equipment castings typically run airflow pre-compaction plus hydraulic multi-piston squeeze compaction at 1.5 MPa max, with 90–95 mold hardness, CNC/PLC control, and component brands including Siemens, SEW, Rexroth, and Schneider. Apply this line to batch duc

Die casting machine spare parts split into wear consumables (shot sleeves, plunger tips, ladle cups, die spray) and capital spares (tie bars, platens, goosenecks, hydraulic valves, PLC cards). Buy machine-specific consumables from the OEM channel, source structural spares from component rebuilders,

Gas-fired reverberatory aluminum melting furnaces for rail components typically operate at 1,160–1,210°F melt range, with 10:1 bath-to-melt ratio and capacities from 300 lbs crucible to 300,000 lbs bulk holding. Selection hinges on melt rate, alloy purity, and refractory design, with dry hearth pref

Pump and valve foundries running induction furnaces lose coils, crucibles, and entire melts to three repeatable failure modes: fouled cooling water, vacuum leaks, and neglected refractory. Targeted maintenance on those three systems stabilizes uptime and protects pump/valve casting quality.

A die casting machine inspection checklist is a structured walk-down of eight systems, die condition, shot, clamping, ejection, thermal, lubrication, cooling, and casting QA, run on cycle-based intervals (not calendar days) to keep molten-metal work above 1,200°F and clamping tonnage over 1,000 t pr

A well-maintained die casting machine typically delivers 15-25 years of service, with rebuilding extending life at 30-50% of new cost. Replacement beats rebuild when electronics are obsolete, safety standards lapse, or downtime exceeds 15% of operating time. Specification focus on preventive mainten

Casting-mold specification for hardware manufacturing hinges on three choices: process family (sand, permanent, die, investment), mold-base steel grade (e.g. H13, 45 medium-carbon), and a part envelope from under 1 oz to about 400 lb. Permanent mold typically hits 100 RMS surface finish; HPDC uses p

Zinc die casting machines running electronics-housing tooling at 1.5 mm wall sections stay reliable with three maintenance pillars: thermal control within ±5°C, scheduled hydraulic and lubrication discipline, and predictive sensor monitoring. A 200-ton hot-chamber cell casting a 420 g Zamak 5 enclos

Sand reclamation unit commissioning follows a fixed sequence: bench test of feed sand, mechanical dry-run, thermal or pneumatic ramp to design temperature or scrubbing energy, and acceptance run at 95% reclaimed/5% new sand blend.

A die casting machine forces molten non-ferrous metal into a hardened steel die cavity at 7–350 MPa, solidifies the part under maintained pressure, then opens to eject. Hot-chamber units suit low-melt alloys like zinc; cold-chamber machines handle aluminium and magnesium above 650 °C.

A deburring machine removes metal burrs, slag, and sharp edges left by stamping, milling, drilling, laser, or plasma cutting using mechanical abrasion, vibratory media, thermal energy, or electrochemical dissolution. Selection hinges on burr type, material, geometry, and required edge finish.

A parts washer removes oil, grease, metal chips and residues from workpieces using heated aqueous detergent, solvent immersion, high-pressure spray, or ultrasonic cavitation, with the four Sinner factors (time, temperature, chemistry, mechanical action) governing cleaning result. Aqueous alkaline sy

Deburring machine specs center on burr type, abrasive grit (P36 to P180), edge-rounding radius (up to 2 mm), and throughput mode (batch vibratory vs. single-pass belt). Aerospace allocates ~30% of part cost to deburring, automotive 15-20%. Selection hinges on burr geometry, material thickness,

Vibratory feeder maintenance follows a daily-to-quarterly schedule: visual and current-draw checks daily, spring and air-gap inspection quarterly, drive-coil insulation testing bi-annually, and full re-tune with load. Fastener torque, spring-leaf fretting, and sub-resonant drive frequency are the th

Install a vibratory feeder by mounting on a rigid, level surface, isolating structure-borne vibration, then powering through an SCR or 3-12 VDC controller after a two-minute warm-up to set steady-state displacement. Mounting, electrical, tuning, and overload are the four failure nodes that decide a

Vibratory feeders move bulk material by combining controlled mechanical vibration with gravity, using electromagnetic, natural-frequency, or out-of-balance drives. Throughput is set by frequency, amplitude, and spring/tray geometry, and capacity spans a few pounds to several tons per hour.

Vibratory feeders are bulk-material handling devices that move parts or granules via controlled vibration, with electromagnetic, natural-frequency, and out-of-balance drive types covering ounces to tons per hour. Specifying one requires matching drive type, tray geometry, vibration frequency, and ca

Hydraulic press maintenance is a tiered fluid, seal, and safety inspection routine: daily leak and gauge checks, monthly filtration service, and a 2,000-4,000 hour oil change, with filtration targets of 10 micron for basic systems and 6 micron for servo or proportional valve circuits.

North American mold base sourcing splits between modular catalog suppliers (DME, PCS, HASCO) shipping pre-engineered 5- and 7-plate assemblies and custom CNC shops (Mac-Mold Base, Cross Tool, Superior Die Set) machining pockets, waterlines, and ejector housings to print. Buyer decision hinges on fra

Standard injection mold bases for plastic parts are stocked in roughly 7.875 in. to 23.75 in. (200 to 603 mm) footprints with plate stacks from 7/8 in. to 5-7/8 in., and selection begins with the molded part's projected area, gate type, slide count, and required ejection stroke. Match the frame size

For pulp and paper mold bases in 2026, machined aluminum dominates short runs and prototyping, while tooled steel wins long-run wear life. Selection pivots on forming pressure, fiber slurry chemistry, and mesh-versus-solid drainage geometry.

Sand casting mold suppliers split into two tiers: industrial foundries producing bronze, iron, and steel castings at 2M+ ton annual scale, and small-flask tool makers selling $13–$119 kits for jewelry and prototyping. Selection hinges on alloy, part size, certification scope, and whether the order i

Sand casting fits parts from roughly 20 g to several hundred tonnes, with flask size as the hard ceiling on green-sand work; green-sand, dry-sand (chemically bonded), and no-bake/loam cover nearly every size and tolerance need in modern foundries.

For aerospace sand casting, green-sand or air-set silica molds paired with aluminum alloys (A356, A357) remain the practical default for large structural components, while 3D-printed smart sand molds target thin-wall, complex-geometry programs where investment casting would otherwise dominate. Sand

Sand casting mold choice hinges on four decisions: sand system (green sand, sodium silicate, or furan resin), molding method (green sand, no-bake, or matchplate), pattern type, and casting-mold vs casting-process trade-offs. Match the choice to part weight, tolerance, surface finish, and run size, n

Aluminum dominates the US die casting market at 57% share, with magnesium the fastest-growing alloy at 8.25% CAGR through 2031. Supplier shortlisting should prioritize IATF 16949:2016 certification, machine tonnage from 60T to 2,500T, and verified multi-alloy capability over company age or size.

For marine duty, select a corrosion-resistant aluminum or zinc-alloy die casting die (A360, A383, ZA-8/Zamak 3/5) with hardened H13 tool steel inserts, multi-slide slides, vacuum venting, and conformal cooling. Target a 1,000-4,500 ton cold-chamber press with shot monitoring.

Choosing a die casting die comes down to four decisions: matching die steel (H13, SKD61, DIN 1.2343) to the alloy being cast, sizing shot weight to the cold-chamber machine's locking force, designing cooling lines for a 2-4 mm wall thickness range, and budgeting for 150,000 to over 1,000,000 shots b

AFC-Holcroft, Ipsen USA, Lindberg/MPH, CEC, Lucifer Furnaces, Grieve, HeatTek and Cooperheat are the established North American heat treatment furnace builders as of 2026-09-11, with Ipsen USA leading at $110M+ 2023 sales. Selection hinges on atmosphere vs vacuum, temperature class, and compliance w

Spec-first heat treatment furnace selection matches furnace class to workload, atmosphere, temperature uniformity, and case-depth target. Box and integral-quench batch units dominate general shops, pusher and walking-beam continuous lines fit high-volume gear and fastener work, vacuum covers clean-s

Air, atmosphere (gas-tight and muffle), and vacuum furnaces are the three furnace families specified for HVAC component heat treatment, with selection driven by alloy grade, surface-finish tolerance, and batch size. Air units suit carbon-steel stress relief, while gas-tight atmosphere and vacuum fur

Riser cutting machine supply in 2026 stays concentrated in Pune and wider Maharashtra, with Stark Automation and Ceratherm Technologies shipping dry-cut, 240V diamond-blade units, plus Jiangsu Tianhong holding a horizontal wheel-hub patent (CN203526528U). Selection hinges on cutter type, motor power

A riser cutting machine is a foundry-specific bandsaw or circular-saw cell used to knock off cast risers, runners and sprues from cylinder heads, pump housings and mining castings; pick by blade diameter, spindle count and clamping logic, not by brand.

Selecting a riser cutting machine comes down to four gates: match the machine variant to your casting family, verify spindle power and cutting speed, confirm fixture availability for your part geometry, and demand cooling plus guarding for cycle-time stability.

Foundry-grade fettling grinders are dominated by Indian and Chinese OEM clusters offering pedestal and swing-frame units in the 3-15 HP range with 300-600 mm wheels, with 2026 spec sheets converging on 80 m/s rim speed and 5.5-15 kW motors for iron and steel cleaning cells.

A fettling grinder for foundry cleaning cells is sized by three coupled gates: 3.7-11 kW (5-15 HP) motor band, 300-500 mm resinoid-bonded wheel at 1600-2700 rpm, and casting-mass class. Pedestal snagging handles parts under 25 kg, swing-frame covers 25-500 kg, and handheld angle covers sub-1 kg cosm

For chemical processing in 2026, the strongest fettling-grinder candidates are corrosion-resistant industrial granulators (e.g. MPE-style chain-and-roller) for bulk lines, plus planetary ball mills, disc mills, and rotor mills for sample-prep labs, selected by Mohs hardness, moisture, and heat sensi

Choose a fettling grinder by matching wheel diameter (12 to 24 inch) and motor power (3 to 15 HP) to casting weight, then lock the format (pedestal snagging vs swing-frame) to gate mass and booth layout. Spec sheets from Ganesh and Cast Grind Solutions, plus the July 2026 trade-off map, set the real

Sand blasting machine suppliers in 2026 cluster around pressure pots sized 300, 600, and 1000 lb, with US-made ASME-coded vessels rated 150 psi and German/Italian integrators dominating cabinet and robotic lines.

Sizing a sand blasting machine comes down to matching nozzle CFM draw to compressor output: a 7/16" orifice at 90 PSI pulls 240 CFM, while a 5/16" orifice at 50 PSI only needs 77 CFM. Pick the air supply, pot size, and abrasive media around that nozzle-to-CFM relationship, not around the cabinet on

Sandblasting machines for data center builds focus on surface prep for steel structural components, server rack frames, and stainless steel sheet panels, with conveyor, batch, and high-pressure models covering 0.5–50 MPa ranges, 6–30 kW power, and PLC control. Selection hinges on part geometry, dail

Pick a sandblasting machine by matching abrasive media, compressor CFM, and duty cycle to the substrate: siphon or pressure pot for metal, walnut shell or corn cob for wood, wet/dustless for coating-strip work. A 5–8 CFM compressor suits gravity-feed units, while pressure blasters need 15–25+ CFM an

Foundry sand coolers in 2026 are dominated by fluidized-bed designs, with General Kinematics, DISA, Küttner, Palmer, Carrier, and Indian OEMs offering units from 5 to 70 TPH and outlet temperatures as low as 120°F. Selection hinges on throughput, inlet/outlet temperature, moisture control accuracy,

For power-generation foundries burning through tonnes of hot return sand per shift, a vibratory fluid-bed sand cooler with PLC temperature control is the spec-first pick, per Carrier's 2026 published design.

Foundry sand coolers are selected on three hard specs: throughput in t/h, inlet sand temperature (often 120-180°C from shakeout) and target outlet below 30-40°C, plus available floor space, water/electricity budget, and dust compliance under foundry ventilation rules. A spec-first comparison of rota

Foundry shakeout machine suppliers in 2026 span Carrier, Palmer, General Kinematics, DIDION, SINEX and Asia-OEM makers (Galante Sk-series, HSD L12, YSHO, Maith), with vibration classes 1.5–45 kW and deck loads 5–60 kN covering green-sand and no-bake lines. Selection pivots on load class, grate size,

Vibration shakeout machines for green-sand and no-bake foundries span 5–80 T/H throughput, 5–100 t deck loads, and 2×3 to 2×22 kW drive power; sizing hinges on casting mass, sand type, deck area, and exciter class. Match load rating and deck aperture to the heaviest flask, pick natural-frequency or

For automotive-parts foundries running engine blocks, cylinder heads, and suspension arms, the spec-first shakeout shortlist comes down to three gates: sand-to-metal ratio (5:1 to 60:1), casting entry temperature often above 200 °C on green-sand lines, and peak mold throughput with a 1.3 to 1.5 surg

Foundry shakeout selection hinges on sand-to-metal ratio (5:1 to 60:1), mold type (green sand vs no-bake), and casting fragility. Match vibratory drive type and deck geometry to part sensitivity and downstream sand-handling integration.

For semiconductor foundries, pneumatic (mechanical) and thermal sand reclamation units each fit different purity, throughput, and energy budgets. Simpson Pro-Claim pneumatic scrubbers can cut new-sand use to 5% of mix, while thermal units like EnviroAir and Omega Sinto handle 0.25-60 TPH at under $7

Choose a sand reclamation unit by first matching reclamation mechanism (mechanical/attrition, pneumatic, thermal) to the binder system, then by throughput and downstream sand quality. For most no-bake and green-sand lines, a pneumatic or attrition unit between 1 and 30 TPH is the workhorse; thermal

Casting mold sizing and selection hinge on three engineering numbers: the 2 to 5 cm sprue/runner minimum, the cast-material shrinkage rate (1 to 3 percent for plastics, 0.5 to 1 percent for concrete/plaster), and a clear match between mold body and pour medium. Pick the mold family from the pour med

Match the casting-mold material to the alloy, temperature and production volume: silicone for fine resin/wax detail, HDPE plastic for reusable craft molds, and sand, clay-bonded or graphite molds for metal. Confirm alloy family, draft, parting line and pouring temperature before tooling.

Shot blasting machine supply in 2026 is split between long-established Western OEMs (Pangborn, Wheelabrator, Rösler, Viking, BlastKing) and a dense Chinese manufacturing base led by Qinggong with 40+ years of build history. Selection is driven by workpiece geometry, throughput, and abrasive recovery

Shot blasting machine sizing hinges on three coupled variables: workpiece geometry, abrasive media size (S330 to S780 steel shot), and the wheel versus air-blast architecture, with wheel-blast units favored for high-throughput industrial duty and air-blast units reserved for intricate or confined pa

Choosing a shot blasting machine comes down to matching wheel-blast or air-blast architecture, blast width (10-23 in on walk-behind units), turbine power (11-23 HP), and abrasive hardness to your workpiece and surface profile target, with concrete prep favoring 12.6 in / 15 HP walk-behinds and struc

Industrial shell core machines built for HVAC component foundries run 30-120 second cycle times, 4-12 bar blow pressure, and 5-30 lb core weight capacity on dual-station gas- or electric-heated platens. Spec HVAC work on 5-10 kg valve and pump bodies with resin-coated silica sand, 180 degree tool ro

Shell core machine certification centers on ISO 9001 quality system evidence plus 30 Tex. Admin. Code § 106.314 air-permitting compliance for U.S. foundries. Buyers should verify ISO 9001:2015 scope, machine platen/core-weight ratings, and resin-binder emissions controls before procurement.

Shell core machine calibration and maintenance center on three recurring failure modes: core box misalignment, temperature control drift, and mechanical wear on bearings and gears. A weekly inspection interval covering sensor recalibration, vent/coolant clearance, and lubrication holds scrap rates d
Shell core machine datasheets hinge on platen size, core weight capacity, gas pressure and air consumption, with Redford, Shalco, Harrison, Dependable and EMI as common U.S. platforms ranging 40-370 lb cores on platens from 13x15 to 36x44 in.

India-led suppliers dominate the shell core shooter market in 2026, with horizontal and roll-over PLC machines handling 5–20 kg cores at 4–6 bar blow pressure, 440 V 3-phase supply, and electric heating up to 250°C for foundries worldwide.

Shell core shooter sizing is governed by core weight, core-box dimensions, and parting orientation, with commercial models spanning roughly 3 kg to 100 kg shot capacity. Selection should match sand/binder system, automation level, and the 415 V / 3-phase utility supply standard on pneumatic-hydrauli

Shell core shooters built to oil-and-gas valve, manifold, and downhole-tool casting standards require 4–6 bar blow pressure, electric core-box heating at 440 V 3-phase, and 10–20 kg shot capacity with PLC or SCADA control. Kelsons, Makewell, and Shalco platforms cover the 3–100 kg core-weight band u

Shell core shooters cure resin-coated sand in a preheated core box to 250 C, producing thin-walled cores with controlled shell thickness for iron, steel, and aluminum castings. Match the machine class (top-shoot, swing-door, roll-over, two-station) to core weight, plate size, and batch volume.

Hot box core shooters size resin-coated sand cores in heated tooling at 250 to 350°C, with small-to-medium machines capping near 500×500×400 mm core boxes. Selection hinges on core mass, shot pressure band, and tooling match, not marketing cycle claims. Match machine class to the heaviest core in th

Hot box core shooters cure phenolic resin-coated sand at 250-350°C with shooting volumes of 10-150 L, but pulp and paper foundries rarely justify the investment: paper-machine castings favor cold box or larger shell processes, with hot box reserved for small-to-medium valve and pump cores under 80 L

A hot box core shooter cures phenolic resin-coated sand at 250-350°C box temperature with 0.2-0.4 MPa blow pressure, suiting small-to-medium cores for automotive, valve, and machinery foundries needing fast cure, low toxic emissions, and complex internal cavities.

Cold box core shooter sourcing in 2026 spans Indian cluster suppliers (Kolhapur-based Ganesh Quality Machines, Vijay Foundry Equipments, Alcast) and Chinese OEMs (ATHI, Kao Kuo, EMP, Harrison, Omega, Pangborn, Qingdao Aoqiang), with core weight classes from 5 kg bench units to 150 kg horizontal mach

Cold box core shooters are sized first by core weight and parting geometry (typically 3-100 kg capacity, horizontal, vertical, or universal), then by shot pressure range, gassing uniformity, and tooling changeover. Buyers should match shot chamber volume to the heaviest core, not average output, and

Fettling grinders for pump and valve production are heavy-duty abrasive machines used to clean castings, dress weldments, and finish flow-control components. Selection turns on workpiece geometry, stock removal, abrasive spec, and dust extraction class, not brand loyalty.

Cold-chamber aluminum die casting machines, sized 160–1,600 tonnes clamping force, dominate hardware manufacturing where high-melt alloys (Al, Mg, Cu) are specified; hot-chamber and vacuum units fit lower-volume, lower-melt hardware lines.

Aluminum cold chamber die casting machines in the 500-1,200 ton clamp range, paired with A380/A360/B390 alloys, are the dominant build path for agricultural gear housings, pump housings, fan blades, and equipment covers, replacing iron and steel weldments at roughly one-third the weight.

For pump and valve bodies, cold-chamber aluminum die casting with 800-1600 ton clamp force, vacuum assist, and squeeze-pin porosity control delivers the leak-tight castings this category requires. Match tonnage to projected area, shot weight to part mass, and verify ISO 9001:2015 plus pressure-tight

Aluminum high-pressure die casting at 7–350 MPa injection pressure and 250–2400 tonne locking force is the dominant process for LED heat sinks, streetlight housings, and outdoor brackets, with cold-chamber machines in the 88–500 ton class most commonly specified for lighting parts.

For telecom enclosures the right degassing and refining unit is a small-footprint vacuum or rotary-injection module sized to 50–500 L/h melt, paired with ATEX/IECEx-certified vapor control for enclosure cleaning. Specs to fix: hydrogen target under 0.10 ml/100 g, rotor speed 350–600 rpm, gas-to-meta

Sandblasting machine selection for energy equipment hinges on matching cabinet class, abrasive media, and pressure band to substrate and weld-prep requirements. Stationary dry units held 64.4% product share in 2024, with semi-automatic units at 43.4% of the operation segment. Power-station and subst

Rail-component foundries pair a dedicated casting ladle with the part geometry and iron grade they pour: small hand-shank ladles for short-run castings up to ~20 kg, geared crane ladles for serial production, and refractory-lined transfer or treatment ladles for ductile and austempered ductile iron.

Industrial oven selection starts from the process envelope: required min/max temperature, batch geometry, airflow, atmosphere and utility limits, not the brand. Match the oven family (batch chamber, walk-in, tunnel/conveyor, conveyor-belt, or continuous Catenary-style line) to your loading method, f

For rail components, select a gravity die casting machine when the part must carry load after T6, the run sits between sand and high pressure die casting volume, and A356-T6 (290 MPa tensile, 4% elongation) is acceptable. Specify tilt-pour, 200–300 °C mold preheat, and a permanent steel die.

Cold chamber die casting machines are the standard pick for aluminum and magnesium electronics housings above roughly 90 g shot weight, where hot chamber systems hit thermal limits on the gooseneck. Selection turns on tonnage, shot weight, alloy grade, and cycle-time acceptance.

Spec an outdoor telecom cabinet by site profile, not by catalog page: aluminum 5052/5754 is the default, 316 stainless is non-negotiable within 5 km of coast, and IP rating alone won't stop condensation above 90% RH without active thermal management.

For aerospace aluminum die casting, select a high-pressure cold-chamber machine rated 800–4,000 tonnes clamping force, with vacuum assist and a shot sleeve sized to 30–50% of the projected cavity area. A380/A360 alloys dominate non-flight-critical housings; primary load-path parts need forging or ma

Gravity die casting (GDC) machines, filling moulds at 0.1–0.5 m/s under gravity alone, suit energy equipment parts from 150 g to 200 kg in aluminium, copper alloy, and cast iron where air-tightness and heat-treatability outweigh thin-wall speed. HPDC is faster but porosity-prone; LPDC (2–15 psi) is

Aluminum die casting machines for automotive parts are selected on tonnage class, shot weight, cycle time, and alloy family; cold-chamber HPDC dominates structural and powertrain work, while hot-chamber machines cover zinc brackets under ~1 kg.

Gravity die casting machines suit telecom enclosures when production runs are low-to-medium, wall sections exceed 3 mm, and T6 heat treatment is required. A356-T6 alloy hits 290 MPa tensile and 4% elongation, and a tilt-pour permanent mold yields dense, low-porosity housings that are well-suited for

Industrial parts washer suppliers in 2026 split into three tiers: aqueous-system specialists (Better Engineering, Niagara Systems), solvent and ultrasonic vendors (Best Technology, Graymills), and service-based programs (Crystal Clean). Selection hinges on part geometry, cleanliness spec, throughput

Aluminum sheet and aluminum die casting are two different forming routes for the same base metal, with sheet suited to flat stock from 0.2–6.0 mm and die casting reserved for complex 3D geometries produced on presses from 400 to 1,200 tons clamping force. For high-volume, net-shape parts under 25 lb

Foundry sand reclamation falls into three families: mechanical (dry attrition), wet, and thermal (typically above 600°C), with chemically bonded systems often staged as primary attrition, secondary attrition, and thermal. Selection is driven by binder type, AFS grain size stability, and the foundry'

A shell core machine installation covers six steps: site prep, utility hookup (gas/electric/air), leveling, core box mounting, HMI commissioning, and cure-temperature calibration on heated platens. Skip the foundation or ventilation work and the resin-coated sand will not cure evenly, and the machin

Fettling grinders divide into five format classes: handheld angle, pedestal/snagging bench, swing-frame, double-ended pedestal, and robotic cell, spanning 0.3-15 kW, 4-24 in wheels, and 80-3821 rpm. Spec gates are wheel size vs motor power, spindle-rpm vs rated-rpm match, ATEX/IECEx zone rating, and

Sand blasting machine total cost of ownership is driven by five line items beyond purchase price: abrasive media, compressed-air energy, nozzle and wear-part replacement, maintenance labor, and dust-collection compliance. Across industrial plants, the air utility alone can swing 30-50% of lifetime c

For telecom enclosures, specify an LKM/HASCO-class standard mold base with P20 or 2738 steel, single- to 4-cavity layout, hardened leader pins, and cooling channels matched to ABS, PC, or PC/ABS resin flow. Match frame size to part projected area, and tie ejection to thin-wall draft rather than to p

For electronics housings, choose a standard 7-plate A-Series or compact 5-plate B-Series mold base sized 7.875 x 7.875 to 23.75 x 35.5 inches in No.1/No.3/No.7 pre-finished steel, matching ejector and guide layout to boss and connector geometry before specifying flame-retardant resin grades and wall

Standardized mold bases for energy equipment run on P20/1.2311 at 28-32 HRC (clamping plates), SUJ2 guide pillars at 58-62 HRC, and a 5- or 7-plate stack-up sized 250x250 mm to 800x800 mm; DME, HASCO, and FUTABA interchangeability governs component fit across injection-molded busbar insulators, swit

Mold base selection in hardware manufacturing hinges on plate stack, steel grade, and lifecycle cost, not just purchase price. Standard P20 or 1045 assemblies under 10x12 inches typically run $500 to $1,500, while 18x24 inch multi-plate bases reach $1,500 to $5,000 USD.

Selecting a mold base for pump and valve production starts with matching the SPI class to cycle count, choosing standard versus custom frames, and verifying steel grade plus hardness against cavity and core requirements.

For agricultural injection-molded parts, mold base selection is driven by machine tonnage, shot volume, cavity count, and field-service resin choice (UV-stabilized PP, glass-filled nylon, ABS). Standard H-type or I-type bases cover most farm-equipment tooling.

Automotive mold base selection hinges on steel grade, plate-stack size, and ejection/guide layout: DME A-Series spans 7.875x7.875 to 23.75x35.5 inches across 9 plate thicknesses, while frame steels fall into three families (hot-rolled, chrome-moly, stainless) matched to part size, resin, and cycle.
Rail components favor green sand or dry sand molds: green sand is lowest cost for high-volume brackets and housings at 1000-5000+ units/year, dry sand (chemically bonded) handles thick steel bolster and side-frame sections above 100mm and hits tighter linear tolerances of +/-0.4-0.5mm.

Green sand and resin-bonded sand molds remain the workhorse for energy-equipment castings, with green sand handling 60% of all metal castings and resin sand used for intricate cores. Selection pivots on alloy, geometry complexity, and post-machining tolerance rather than cost alone.

Sand casting is the workhorse for telecom enclosure prototyping and low-to-mid volume runs under ~500 pieces/year, with aluminum alloys, ASTM A216 grades, and ductile iron covering the bulk of base station and antenna-mount specs. Process choice between green sand, no-bake, and 3D-printed sand molds

For lighting fixtures, green-sand and dry-sand (chemically bonded) aluminum molds remain the workhorse, with permanent mold and die casting stepping in at higher volumes. The decisive selection variables are volume, dimensional tolerance (typically +/- 1 mm, down to +/- 0.4–0.5 mm on dry sand), mini

Sand casting mold selection for hardware manufacturing hinges on four gates: production volume under 500 pieces per year, alloy range (Al, Zn, Fe, steel, bronze), sand system (green sand vs resin-bonded vs sodium silicate), and ISO 8062 tolerance grade. Match these before pattern material, draft, an

Green sand, resin-bonded (no-bake), and shell sand molds are the three principal routes for pump and valve castings, with selection driven by part size, alloy, and required surface finish. Ferrous foundries routinely pour valve bodies and pump housings in over 100 iron and steel grades, with floor m

Sand casting mold selection for agriculture machinery is governed by four gates: iron alloy grade, sand system (green vs resin), pattern complexity, and batch size. Gray and ductile iron dominate tractor housings, gearbox bodies, and axle supports, with ferrous foundries casting single parts up to 6

Aerospace sand casting mold selection balances alloy family, sand system, and process route. Green sand suits large structural parts, resin and shell systems deliver tighter tolerances for engine and turbine components, and 3D-printed sand molds unlock thin walls above 7% projected market CAGR throu

Sand casting molds remain the default route for automotive engine blocks, cylinder heads, transmission cases, and suspension knuckles, with aluminum and iron alloys dominating 2026 sourcing. Selection is driven by part size, run volume, alloy, and required draft, not by tolerance alone. Green sand f

Aluminum die-casting dies for telecom enclosures are selected around five gates: alloy (A380/A383/ADC12), shielding-grade steel (H13/SKD61), tolerance class (±0.05 mm), IP67 sealing surface, and EMI/RFI shielding continuity. Die-cast housings beat extrusions for 5G base-station, RRH, and antenna-int
For electronics housings, die selection is driven by four hard gates: alloy family (Al, Mg, or Zn-Al), minimum wall thickness, cavity count, and rated tool life. Aluminum HPDC dies in H13/8407/SKD61 rated 30,000 to 100,000+ shots on 350T-3000T machines are the default, while magnesium thin-wall prog

For 2026 lighting-fixture programs, die-casting die selection hinges on alloy, projected area, and annual volume: aluminum (ADC12/A380) cold-chamber dies in the 160-630 t range with H13 or Dievar inserts above HRC45 drive LED heat-sink and street-light housings, while hot-chamber zinc dies in the 50

For hardware manufacturing, a die casting die is specified by locking force (1000-4000 kN), H13 tool steel at 44-52 HRC, and 100,000-500,000 shots life; pick cold-chamber for aluminum, hot-chamber for zinc, with gating velocity 30-45 m/s and vacuum assist for thin-wall Class 2 radiographic parts.

Die casting die selection for pump and valve production is governed by four hard numbers: alloy chemistry, projected area, clamping force, and shot life. Cold-chamber HPDC at 400-8800 t covers aluminum pressure die casting; hot-chamber covers zinc and magnesium under roughly 420 °C; gravity die cast

Specifying a die casting die for agriculture machinery in 2026 reduces to four binding numbers: tolerance band (typically ±0.005 to ±0.03 mm), mold steel hardness (HRC >45 to 54-56), cycle life (45k to 135k+ shots), and alloy-grade fit (A380, A356, ADC12, AZ91D). Buyers should reject any agricultura

Aerospace die selection locks in four hard constraints first: alloy (A380/AZ91D/ZL101A), annual shot count, tolerance band, and surface finish, then die steel, gating, cooling, and ejection follow. Cold-chamber H13 dies for aluminum and magnesium target 100,000-250,000 shots; zinc hot-chamber P20+Ni

For telecom enclosure heat treatment, a 60-250 °C box-type resistance or muffle furnace is the correct match, not a 1100-1500 °C crucible or melting unit. Specify ±3-5 °C uniformity, a full-fiber lining, and a low W/L heater density to protect gaskets, PCBAs, and coatings during bake-out and stress-

Vacuum and controlled-atmosphere furnaces are the default choice for electronics housings made of aluminum or precision steel, with operating windows typically between 250°C and 1300°C depending on alloy, and ±5°C uniformity being the practical spec floor. Selection hinges on four gates: alloy, surf

Heat treatment furnace selection for hardware manufacturing hinges on four data-driven gates: workload-driven technology, atmosphere control, refractory zoning, and simulation-based commissioning. Forging furnaces target 2,200-2,400°F, while vacuum graphite hot zones reach 3,000°C under inert gas. S

For pump and valve production lines, the dominant 2026 heat treatment furnace selection maps to four work zones: bogie hearth for heavy cast bodies, box furnace for batch shells, mesh-belt quenching for fasteners, and tempering for stress relief. Match furnace type to alloy, temperature window, and

Aerospace heat treatment furnace selection is locked by AMS2750H temperature uniformity (commonly ±3°C / Class 2 ±10°F at 1,950°F), alloy-reactivity atmosphere control, quench-delay ≤5 s, and workload geometry, with aerospace steel/aluminum builds dominating 2026 supplier line-ups.

For automotive parts, furnace selection hinges on part family, alloy, and batch size: mesh-belt continuous furnaces (rated 1100°C, ±5°C uniformity) for fasteners and small gears, vacuum gas-quench (up to 1300°C, 0.8–10 bar N2) for high-stress gears and bearings, and pit or sealed quench furnaces for

For energy-equipment foundries, riser cutting machine selection in 2026 hinges on matching 50-500 kN hydraulic shear force or 300-600 mm abrasive wheels to riser neck diameter and melt type, with CE Machinery Directive 2006/42/EC, ISO 12100, and OSHA 29 CFR 1910.95 as the non-negotiable compliance b

For electronics-housing die castings under 150 mm riser-neck diameter, hydraulic-piston shear or abrasive-wheel riser cutters running at 200–400 cuts/h beat manual grinding on cost-per-cut and OEE. Match the cutter to alloy, neck size, and dust-extraction capacity before quoting.

A riser cutting machine is a foundry-specific shear that removes sprues, risers, and feeder heads from castings after shakeout, with hydraulic-piston, servo-CNC, and abrasive-wheel architectures suited to different neck diameters, cycle rates, and alloys. Spec selection hinges on five gates: drive t

Aerospace foundries should treat a riser cutting machine as a spec-driven purchase, not a commodity buy: hydraulic shear units (10–21 MPa, 5–30 kN) suit large aluminum and steel aerospace castings up to 250 mm riser neck, while servo-CNC cells with ±0.5 mm repeatability are the right pick above 1,50

Riser cutting for automotive parts runs on three abrasive platforms (cut-off wheels, CNC saw bands, and rotary/flatbed die tooling) selected by stock size, alloy, tolerance, and volume. Cut-off wheels handle gates under ~50 mm; CNC saws cover 10 mm to 4000 mm blanks at ±0.1 mm tolerance; die cutting

Fettling grinders for electronics housings diverge from foundry snagging duty: housing alloys are thin-wall aluminum or zinc die castings with 0.5-3 mm gates, so a 3-7 kW bench grinder with 300-400 mm wheels and fine-grit aluminum-oxide wheels typically outperforms a swing-frame unit, with abrasive

For hardware manufacturing, pick a fettling grinder on three gates: 12-24 in wheel diameter, 3-15 HP motor (2.2-11 kW) matched to casting mass, and ATEX/IECEx Zone 21 rating where aluminium or magnesium runs through the cell. Two formats compete, pedestal/snagging (3-10 HP) for small-to-medium parts

Rail component foundries should pick sandblasting machines by matching part geometry and rail-grade cleanliness to machine class: roller-conveyor or hook-type shot blasting for 0.5–12 m rail sections, automated wet-blast cabinets for thin-web bolsters. Use 0.6–1.0 MPa air, 20–80 mesh steel grit, and

Hook-type or small crawler sand blasting machines with 11-15 kW blast wheels at 60-80 m/s are the 2026 spec answer for telecom-enclosure surface prep, hitting Sa 2.5 to Sa 3 cleanliness and 50-100 micrometer anchor profile on 5-50 kg thin-wall castings.

For electronics housings (Al/Mg alloy, PC/ABS, stainless steel mid-frames), specify suction or low-pressure automatic sandblasting machines at 0.2–0.6 MPa with 120–240 mesh glass beads or fine ceramic; choose wet systems when dust ≤10 mg/m³ is required.

For lighting fixtures, a suction-type cabinet or wet blasting unit at 0.3–0.5 MPa with 100–240 mesh glass beads is the default pick; pressure-feed and rotary-tumbler systems are reserved for heavier steel housings or batch volumes above the 50–60 cm workpiece band. Match cabinet interior to the larg

For pump and valve production, hanger shot blasting machines are the default for large cast bodies, while tumble or cabinet systems handle small bulk parts; selection hinges on part size, batch volume, surface sensitivity, and abrasive type.

Agricultural machinery sandblasting hinges on matching machine type (pressure pot vs siphon vs wheel-blast) to part profile, with 25-50 CFM compressor support for professional work and media recycling for total cost of ownership.

For aerospace-component sandblasting, specify a sealed cabinet or blast-room system with 0.2–0.8 MPa controllable pressure, boron-carbide nozzles, HEPA dust extraction, and a non-silica abrasive such as glass beads or aluminum oxide, matched to surface-cleanliness and roughness targets rather than g

Rail component foundries running 60-100 TPH resin-bonded lines should default to vibratory fluid-bed sand coolers, because they hit the 49°C / 10°C-above-ambient outlet target with ±0.3% moisture control, while counter-flow rotary units cost USD 70,000-120,000+ at that throughput class.

Fluidised vibro and indirect water-cooled sand coolers sized 5-260 t/h dominate foundry tender specs in mid-2026, with discharge sand temperature held at ≤30-50°C. Selection hinges on cooling duty, media type, footprint, and dust-extraction integration.

Telecom outside-plant enclosures need closed-loop cooling (air-to-air heat exchangers or vapor-compression A/C) sized to internal heat load plus solar gain, paired with NEMA 4 or 4X cabinets. Choose vortex coolers only when compressed air is available and ambient stays below equipment limits.

Sand cooler selection for electronics housing foundries hinges on matching a two-stage evaporative cooling duty to 100–150°C shakeout sand, with ISO 9001, IP66, and CE/RoHS compliance as baseline gates. Jobbing shops running aluminium motor, battery, and electronics enclosures benefit from buffering

Foundry sand coolers and LED COB heat sinks solve different problems and rarely cross over. A lighting fixture plant that needs a sand cooler is almost always running a metal-casting line, not extruding aluminum, and selection hangs on TPH, ΔT, and the 1.6–2.2% moisture band.

Fluid-bed vibratory sand coolers sized 40 to 100 TPH with 1.6 to 2.2 percent outlet moisture (±0.3%) are the dominant spec for green-sand foundries feeding 60 to 80 TPH resin lines; rotary drum and indirect batch units fit lower tonnage, very dry reclaimed sand, or oxygen-sensitive dust.

Foundry sand coolers sized at 40 to 350 TPH use evaporative cooling to drop shakeout sand from over 1,000°F to about 120°F while holding moisture at 2.0 to 2.2% ± 0.2%, which is the same coupled heat and moisture control that agricultural-machinery foundries must meet for tractor and harvester casti

Fluid-bed sand coolers sized at 40–100 TPH per unit are the practical default for aerospace-component foundries, holding outlet temperature below 49°C and moisture at 1.6–2.2% ±0.3% across 40–100% inlet swings.

Foundries producing automotive iron castings should select a sand cooler sized at 20 to 100 t/h that drops shakeout sand from 100 to 150 degrees Celsius to below 50 degrees Celsius, with discharge moisture held to 1.6 to 2.2 percent plus or minus 0.2 to 0.3 percent. Fluidised-bed and rotary drum des

A shakeout machine for energy equipment must be selected on dynamic-force profile, separation duty, and downstream structural-load limits, because low-frequency vibration from these machines travels through building structures and foundations. Two distinct meanings of "shakeout" exist in 2026: found

Shakeout machines for telecom-enclosure foundries in 2026 are sized by flask-plus-casting mass, sand type, and drive topology, with mechanical inertia units dominating, 15-45 kW mid-band power, and 85-110 dB(A) noise driving enclosure retrofits. Select 30-400 tph drum or vibratory deck classes again

Electronics housing castings demand shakeout machines that pair low-impact vibration with part-size control under 50 kg. Resin-shell and V-process foundries set the process envelope, while low-frequency transmission through plant structures dictates foundation isolation strategy.

For lighting fixture foundries, a shakeout machine is selected by casting-and-flask weight, sand-bond chemistry, and drive topology, with mid-size power draw at 15–45 kW and noise at 85–110 dB(A). Aluminum and zinc cells pair 2-inch rubber decks with vibratory units, while no-bake iron lines step up

Shakeout machine selection in hardware manufacturing hinges on payload (sand-plus-metal mold weight × molds/hour with a 1.3-1.5× peak factor), sand type, and drive topology. Match the vibration class to casting fragility, plan for 85-110 dB(A) noise and dust loading, and right-size 15-45 kW drive po

Pump and valve foundries should size shakeout machines by flask-plus-casting mass first, then sand system, then drive topology. Mechanical inertia units in the 15-45 kW band cover most pump-housing and valve-body flows; no-bake lines need higher impact and a matched reclamation route downstream

Shakeout machine selection for agricultural machinery hinges on matching drive layout, vibration mode, and deck material to crop and tree size: tractor-mounted trunk shakers run at 10-12 Hz clamp frequency with 1,500-2,000 mm stroke, while foundry shakeouts use vibratory, drum, or barrel-horse decks

Aerospace-component shakeouts demand low-amplitude, high-frequency vibration decks sized to thin-wall investment-cast and aluminum-alloy parts, typically 5-15 t/h with vibration amplitudes under 6 mm and a cleanroom-adjacent dust envelope. Rotary drum or two-mass vibratory decks outperform grid deck

For automotive-parts foundries, selecting a shakeout machine comes down to casting weight, sand system, and alloy: aluminum cylinder heads and manifolds need high-frequency vibratory units at 15-24 Hz with rubber decks, iron blocks tolerate high-energy grizzly decks, and no-bake lines require matche

For telecom-enclosure foundries, sand reclamation unit selection hinges on PUNB or furan binder chemistry, AFS 50-70 recovered grain targets and 90-95% closed-loop reuse, with thermal units favoured at 700-800 °C. Mechanical reclamation wins on phenolic shell lines below 10 t/day; pneumatic attritio

Foundries casting LED hardscape fixtures like the Kichler 16101/16103 series should size sand reclamation units in the 20-150 t/h range with mechanical-attrition or pneumatic scrubbing, matching binder chemistry to aluminum pour weights of 2-8 kg. Selection pivots on return-sand throughput, AFS/LOI

Foundries selecting a sand reclamation unit in 2026 should match three decision gates: process family (mechanical, pneumatic, or thermal), throughput band of 1-150 t/h, and total reclamation cost of $4-$34/t. Green-sand lines under 10 t/h are served by mechanical-attrition units at $4-$9/t; chemical

Sand reclamation unit selection for pump and valve production hinges on resin binder chemistry, shakeout sand throughput, and AFS grain fineness targets. No-bake phenolic and furan foundries reclaim 70-90% of spent sand, while green sand loops cap at roughly 30-50% before bentonite balance degrades.

Sand reclamation unit selection for aerospace components hinges on matching thermal load, alloy chemistry, and tolerance to the unit's attrition and classification method. V-Process lines reclaim 95-98% of unbonded silica, while bentonite-bonded greensand loops recover 20-30% of new sand per cycle,

Rail component castings (bolsters, side frames, bogie plates, knuckles) are mostly specified in ductile or grey iron via V-process, green sand, or shell molding, with V-process gaining share where surface and dimensional repeatability matter on medium-to-large structural parts. Selection is governed

For energy equipment castings, die casting on 6,000+ ton machines with H13 steel at 46-50 HRC and conformal cooling is the default for EV battery trays (1,200-1,800 mm) and motor housings, while sand and investment routes remain in play for large or superalloy parts.

Outdoor 5G telecom enclosure production in 2026 routes through three mold platforms: high-pressure die casting (HPDC) in ADC12/A380 aluminum for IP67 radio housings, shell molding on 600×500 to 1000×800 mm flask lines for complex iron brackets, and 250 to 2500 ton injection plus structural foam pres

Electronics-housing die casting molds are specified by alloy, cavity count, shot life, and machine tonnage: aluminum HPDC tools in H13/8407/SKD61 deliver 30,000 to 100,000+ shots on 350T to 3000T presses, while magnesium thin-wall molds and zinc-aluminum hybrid tools cover tighter tolerance and high

For lighting fixtures, die-casting molds using ADC12 or A380 aluminum with LKM C50 + P20 bases and H13/Dievar inserts (hardness >HRC45) suit high-volume LED housings, while resin sand molding lines (flask 600×500 to 1,200×1,000 mm, 30-60 s cycle) fit low-volume decorative and pole-base castings in g

Hardware manufacturers should match casting mold selection to four axes: process family (sand, die, investment, centrifugal, plaster), SPI Class 1-5 volume tier, alloy, and surface/tolerance targets. Die casting suits high-volume non-ferrous runs; sand casting dominates ferrous and large-format part

For pump and valve bodies, select the casting process first by pressure duty, alloy, size and internal flow geometry: sand casting for large or heavy-section parts, shell molding for repeatable mid-volume runs, investment casting for intricate small parts, die casting for aluminum/zinc high-volume h

Agricultural-machinery casting-mold selection hinges on matching die life, tolerance and alloy to the part: 50k–135k cycle hot-chamber dies suit pumps and tractor housings in A380/ADC12, while ±0.005–0.03 mm precision gears need hardened 54–56 HRC steel tooling. ISO 9001:2015 and CE are the baseline

Aerospace casting mold selection pivots on four process routes: low-pressure metal molds for ZL101A tube castings at 0.1-0.5 bar, resin sand and shell lines for 250-500 RMS structural housings, investment casting for thin-wall turbine geometry, and high-pressure die casting above 5,000 pieces. The r

Automotive casting mold selection hinges on matching the casting process (HPDC, gravity, sand, low-pressure) to part geometry, alloy, and annual volume, with H13 tool steel and conformal cooling dominating structural aluminum programs. Budget ranges for automotive die-casting tooling sit at $20,000-

For rail components, hanger-type (overhead monorail) shot blasting machines are the standard choice, with chamber diameters of 1,000–4,000 mm, 2–15 blast wheels, and 50,000 kg load capacity. Specify blast-wheel tip velocity (≈78 m/s), separator efficiency ≥99%, and dust emission ≤10 mg/m³ before sig

Shot blasting machine selection for energy equipment is driven by workpiece geometry, abrasive flow per wheel (roughly 100-250 kg/min) and tip velocity (60-100 m/s), with hook or roller-conveyor layouts preferred for fabricated boiler, wind-turbine and transformer housings.

For telecom enclosure parts, hook-type shot blasting machines with 11-30 kW blast wheels, 60-90 m/s wheel velocity, and 380V/415V three-phase supply are the practical 2026 spec, matched to small thin-wall castings under 200 kg per load rather than crawler or roller units.

Electronics housings (aluminium, zinc die-cast, thin-wall steel) need a cabinet or table-type shot blasting machine with fine steel shot or glass bead media, low wheel velocity, and PLC-controlled cycle time to avoid warping and to keep Ra in the 1.6-3.2 μm range. Tumble blast machines, while the wo

Lighting-fixture parts (aluminum lamp housings, steel brackets, thin-wall reflectors, die-cast heat sinks) span a 0.1-30 kg weight range and mix fragile cosmetic surfaces with hard structural faces, so the correct shot-blasting line is either a tumble-belt batch unit under 30 kg/batch or a hook/hang

For pump and valve foundries, a shot blasting machine is selected by matching wheel type, media grade and cleanliness target to the casting material, with ISO 8501-1 Sa2.5 or Sa3 as the dominant spec gate for pressure-boundary castings.

Agricultural machinery shot blasting selection hinges on part geometry and weight: crawler units handle sub-300 kg castings, hook/pass-through Hanger type runs 5 t coils, rotary tables suit small wheels and plate. Match the machine class to Sa2.5 finish, 199 kW total power and dust ≤100 mg/m³ per GB

Aerospace shot blasting selection hinges on four gates: Sa2.5–Sa3 cleanliness, controlled Almen intensity, low-contamination media (steel shot, cut wire, ceramic 0.2–1.0 mm), and ISO 9001/CE/AMS 2430 traceability. Hook, tumble, and rotary table types each cover a different aerospace part geometry an

For automotive parts, hanger-type shot blasting machines fit collision-free workpieces up to 2 t, catenary (overhead conveyor) lines fit high-volume assembly work up to 500 kg, tumble machines fit small batch parts 5-150 mm, and the right pick is set by part weight, batch size, deep-cavity risk, and

Rail-component foundries should size a shell core machine to a 10–30 kg core weight band, 6–7 bar blow pressure, and electric platen heating at 200–260 °C, with dual-station or roll-over architecture for bogie, wheel-center, and brake-housing cores. For cores above 40 kg, a gas-fired heavy platen (R

For telecom-enclosure castings, vertical automatic shell core machines in the 8-25 kg shot class cover 70-90% of 2026 foundry duty, with platen sizes 550x400 mm to 1100x900 mm, cycle times 25-45 s, and 0.4-0.7 MPa shooting pressure governing the selection. Match alloy, draw depth, and lot size befor

Spec a shell core machine by core weight and box footprint first, then resin class, heating duty, and shot pressure, before quoting any brand. For 2026 China-origin units, mid-size 600×500 mm box, 12 kg shot at 0.55–0.7 MPa and 18–30 kW electric heating covers most 500–2,000 cores/day iron foundries

For 200-8,000 pcs/yr agriculture castings in the 0.3-6 kg core band, a vertical shell core machine with 15-25 kg shot, 500x400-600x400 mm platen and 0.4-0.65 MPa shooting pressure delivers the lowest-cost cores; cold-box wins only above 500 pcs/yr and 5 kg core weight.

For aerospace cores in 2026, a shell core machine with 200-280°C heated platens, phenolic or furan binder, ±0.1 mm tolerance, and shot pressure near 0.4-0.7 MPa fits titanium, nickel-superalloy, and stainless flight hardware, while hot-box or cold-box units win only on cycle time or sand collapsibil

For energy-equipment foundries casting valve bodies, pump housings and turbo impellers, a shell core shooter in the 8-25 kg shot-weight band (200-300 C cure, 0.4-0.7 MPa shot air, 9.5-28 kW load) matches the duty; cold-box platforms take over above 100 kg shot weight. Match platen size, heater kW an

Vertical automatic shell core shooters in the 8-25 kg single-shot class cover roughly 70-90% of telecom-enclosure foundry duty, with platen sizes from 550x400 mm to 1100x900 mm, cycle times of 25-45 s, and 0.4-0.7 MPa shooting pressure governing the 2026 selection cut.

Shell core shooters for hardware manufacturing in 2026 commonly deliver 5-20 kg core weight at 4-6 bar blow pressure with 440 V 3-phase supply, 10-45 s cycle times, and PLC/HMI control for resin-coated phenolic sand cores up to 600x600 mm.

For pump and valve production, the right shell core shooter is selected by core weight, blow pressure, mounting orientation, and PLC control, with horizontal 5-10 kg models at 4 bar and 10-20 kg rollover units at 6 bar covering most fluid-handling foundries.

Shell core shooters for agriculture machinery foundries are specified at 5–20 kg core weight, 4–6 bar blow pressure, 440 V 3-phase, with horizontal, vertical, or roll-over mounting selected by part geometry and cycle-time targets.

Aerospace-grade shell cores demand phenolic-resin hot-cure shot pressures of 0.4-0.7 MPa, platen sizes 400-700 mm, and 20-60 s cures. Horizontal machines up to 50 kg or vertical units up to 25 kg cover most turbine-blade and structural-core tooling in 2026 catalogues.

For automotive parts, a shell core shooter is typically specced by core weight (5–20 kg), blow pressure (4–6 bar), and core box mounting (horizontal, vertical, or roll-over) to match gear housings, pump bodies, and valve casings within 600×600 mm patterns. Selection hinges on five concrete criteria:

Hot box core shooter selection for railway castings hinges on a 10–20 kg core weight band, 6 bar blow pressure, and 440 V 3-phase supply; auto shell and roll-over models with 20 kg shooting capacity are the working baseline for bogie, wheel, and brake components.

For energy equipment foundries selecting a hot box core shooter, the dominant 2026 spec envelope is template size 780-1400 mm, electric heating 25-50 kW, blow pressure around 6 bar, and 10-40 kg core weight on 200-300 kg sand buckets, matched to valve, engine, and power component cores.

For telecom enclosures, hot box core shooters work best below 500 cores per shift; above that, shell or cold-box shooters with PLC control win on cycle time and binder cost. Specify 0.5-0.7 MPa shooting pressure, 380 V/50 Hz power, and ISO/CE certification.

Hot box core shooters cure resin-coated sand at 200–260 °C in 25–60 s per shot, with 5–50 kg shot weights for lighting-fixture foundries. Selection hinges on shot weight, heating power, sand tank capacity, and clamping force. Selva Lakshmi and similar manufacturers supply 3–25 kg machines with 6–14

Hot box core shooters with PLC-controlled 4-6 bar shooting pressure, 12-20 kg capacity, and 440 V 3-phase supply are the standard selection for pump and valve foundries producing thin-wall, complex sand cores. Match machine capacity to core weight class and verify resin compatibility before quoting.

Hot box core shooters for agriculture-machinery castings run on 440 V 3-phase, 4-6 bar blow pressure, 5-20 kg core weight, and 20-120 molds/hour class throughput. Cold box suits medium-to-large runs, hot/shell box suits short-cycle precision cores.

Hot box core shooters for automotive castings run on 440 V 3-phase power with electric core-box heating, 4-6 bar blow pressure, and 5-20 kg shooting capacity, suiting cylinder heads, valve bodies, and pump housings. Selection hinges on core weight, parting direction, and PLC control class.

Cold box core shooters selected for hardware manufacturing should match resin-bonded sand output to three drivers: core size and weight envelope, daily shot count, and amine gas extraction compliance. The cold box process, which uses polyurethane resins hardened by amine gas catalysts, sets the main

Cold box core shooters using phenolic urethane binder and amine gas catalyst are the default route for pump and valve foundries, with ceramsite sand enabling 30 to 50 percent resin reduction and sub 0.15 percent thermal expansion versus 1.3 percent for silica.

Phenolic urethane cold box core shooters deliver the fast amine-cured cycle agricultural-machinery foundries need for thin-wall, high-strength iron castings. For 5-20 kg cores, specify 4-6 bar blow pressure, 440 V 3-phase power, and horizontal core-box mounting. Cold box wins on cycle time; shell ho

Cold box amine (PUCB) core shooters in the 15-50 kg core weight band, with multi-port gassing and hydraulic clamping, are the dominant spec for aerospace sand-core production. A 5-7 kg/cm² pneumatic supply, PLC amine/CO2 purge sequencing, and 3-5 gassing ports are baseline requirements for 10 kg+ ae

For automotive cylinder heads, engine blocks, and complex hollow castings, a cold box core shooter in the 5-25 kg/core range with 5-7 bar shot pressure, 40-60 s cycle, and a phenolic urethane binder delivers the cleanest cores. Vertical-parted machines suit deep undercuts, horizontal-parted units fi

For rail components like bottom bolsters and side frames, specify a V-Process line with a 3100x1900x450/450 mm or 3100x1900x350/550 mm flask, Ra 6.3-12.5 micron finish, CT7-CT9 tolerance, and a vacuum hold of 50-100 kPa using 0.05-0.20 mm EVA/LDPE film.

For energy equipment castings, a V-Process vacuum molding line is built around a 50-100 kPa vacuum holding range, 0.05-0.2 mm plastic film, and airtight flasks; specify it for large clean steel components like turbine housings, valve bodies, and pump casings, not for short-run small parts or high-mi

Electronics housings are best run on thermoforming lines (ABS 150–170°C, PC 180–210°C) rather than V-Process vacuum molding, which targets 50–100 kPa dry-sand metal castings. Specify a V-Process line only for metal enclosures or heat sinks; pick thermoforming for plastic shells.

V-Process (vacuum sealed molding) lines are specified for hardware castings when production needs binder-free sand, Ra 6.3-12.5 µm as-cast surface finish, and ±0.2-0.5 mm/25 mm tolerances. Selection is driven by pattern size, vacuum pump capacity (50-100 kPa differential), and film-handling throughp

V-Process (vacuum sealed molding) lines are a credible fit for pump and valve foundries needing binder-free sand, 50-100 kPa vacuum holding, and Ra 6.3-12.5 µm as-cast finishes, but only above roughly 50-100 castings per shift where flask, film, and vacuum-pump capex pays back. Spec the line on four

For agricultural machinery castings, a V-Process vacuum molding line is best matched to medium-to-large wear parts and short-to-medium runs, where its unbonded-sand mold halves and plastic-film pattern yield clean surfaces without chemical binders, though its 1.0-1.5 ton flask ceiling and pattern-fi

V-Process vacuum molding lines use dry unbonded silica sand held at 50-100 kPa vacuum under 0.05-0.2 mm plastic film, delivering Ra 6.3-12.5 µm as-cast finishes, ±0.2-0.5 mm/25 mm tolerances, and near-100% sand recyclability. Aerospace primary structure is a poor fit; secondary brackets, housings, a

V-Process vacuum molding lines use 50-100 kPa vacuum on binder-free silica sand, hitting Ra 6.3-12.5 µm as-cast finish and ±0.2-0.5 mm/25 mm tolerances. For automotive parts, select flask size, pump capacity, and film gauge first, then verify pattern venting and cycle time against the casting envelo

For energy-equipment castings, a resin sand molding line delivers 400-700 MPa ductile-iron grades and complex thin-wall geometry at 0.3-0.5% scrap, outperforming green sand on surface finish and dimensional control. Match the line to part weight, alloy family, and annual volume before choosing autom

Resin sand (no-bake) molding lines suit telecom enclosure castings when batch volume is low-to-medium and dimensional accuracy matters more than cycle speed. Selection turns on binder family, flask size, sand reclamation rate, and tolerance grade rather than tonnage alone.

Resin sand molding lines fit electronics housing programs only at the 100–5,000 unit/year prototype and bridge-production window, where tooling cost is held to roughly $200–2,000 per pattern and a furan or phenolic binder is chosen to meet UL 94 V-0 flame targets without the cycle-time penalty of di

Resin sand molding lines are specified for lighting-fixture castings that need tighter dimensional tolerance, smoother surface finish, and lower draft than green-sand lines can deliver, with selection driven by batch size, alloy, and surface class. HT200/HT250 gray iron and A356 aluminum dominate th

Resin sand molding lines selected for hardware manufacturing should match resin-sand sand grain distribution and furan/phenolic binder control, with tolerance targets of CT8–CT10 (ISO 8062-3) and surface roughness Ra 12.5–25 µm. For volumes above ~5,000 pieces monthly, automated flaskless molding li

Resin sand molding lines (furan-bonded, 1.2–1.6% resin, CT8–CT9 by ISO 8062-3) suit pump and valve bodies from 0.05 kg to multi-ton castings at 3,000 t/month capacity. Specify line by part weight, alloy, batch size, and required tolerance before choosing auto vs manual.

For agricultural machinery castings weighing 20 to 500 kg with complex geometry and tight tolerances, resin sand molding lines deliver ISO 8062 CT7 to CT9 accuracy and Ra 3.2 to 12.5 micrometer finishes, outperforming green sand on precision while undercutting shell molding on unit cost. Selection s

Resin sand and shell molding lines suit aerospace brackets, valve bodies, and superalloy housings where 250-500 RMS finishes and CT7-8 precision are acceptable, but investment casting or VIM superalloy routes outperform on thin-wall turbine and flight-critical geometry. Select a no-bake resin line f

Resin sand molding lines suit automotive parts runs of 500-50,000 pieces where dimensional repeatability under +/-1.5 mm and medium-to-heavy iron/steel grades are required, outperforming manual lines on cycle consistency. For sub-500-piece prototype or short runs, a manual line paired with shell mol

Shell molding machines for rail component castings run on 5-50 kg shot weights with 600x500 to 1200x1000 mm platens, 200-280 deg C pattern temperatures, and 0.4-0.6 MPa cure air, prioritizing wear resistance and dimensional stability over surface cosmetics. Selection hinges on shot weight, platen si

Shell molding is a poor fit for thin-wall electronics housings under 3 mm: cycle time and resin-flexibility constraints favor injection molding with UL94 V-0 ABS, PC, or PC/ABS. Shell molding fits only heavier electronic structural brackets, heat sinks, and motor frames where metal cast iron or alum

Shell molding machines sized 15×20″ to 30×44″ with 500–600 mm flask capacity are the standard match for pump and valve body production, balancing thin-wall detail against cycle time. The right pick depends on flask size, alloy range, and whether the line integrates with investment casting for high-f

Shell molding machines sized 15×20" to 30×44" fit agriculture castings like gearboxes, sprockets, and pump housings when runs hit medium-to-high volume. Grey or ductile iron is the dominant alloy; coated-sand shells, MAGMASOFT simulation, and in-house CNC machining are the recurring 2026 buying sign

Shell molding machines for aerospace components typically run on resin-coated silica sand, target tolerances near ±0.1-0.2 mm, and pair with thermosetting resin-shell molds qualified to AS9100 supplier programs for medium-to-high volume precision castings.

Shell molding is a precision fit for automotive parts under 80 kg at volumes above 1,000 pieces, delivering tighter tolerances than sand casting at lower cost than investment casting. Selection hinges on part weight, alloy, tolerance band, and required shell-molding machine class.

Lost foam casting delivers ±0.5–1.0 mm tolerance for rail bogie brackets, wheels, and structural castings in ductile iron and carbon steel, with unbonded sand recycled at ~98%. Specify it for medium-to-high volumes in those alloys; avoid it for stainless, heat-resistant grades, or prototypes.

Lost foam casting lines cut defect rates from 8-15% in green sand to 2-4% for gray and ductile iron in the 5-200 kg range, while delivering ±0.5-1.0 mm tolerances that reduce CNC stock removal by 40-60%. For energy equipment housings, valve bodies and pump castings, a properly specified 50-5000 t/yr

For telecom enclosures, a lost foam casting line is selected around four coupled spec gates: EPS pattern density 18-25 kg/m³, refractory coating dry film 0.8-1.5 mm, flask vacuum 0.04-0.07 MPa, and molding throughput matched to annual volumes of 50-5,000 pieces. This profile suits ductile iron and a

Lost foam casting lines sized for lighting fixtures must hit three numbers: pattern density 18–25 g/L, daily output 1,500–3,000 EPS patterns, and tolerance ±0.5–1.0 mm, per current EPC and foundry guidance.

Lost foam casting lines are best selected against verified tonnage, pattern-cycle math, and a 2-4% defect window, not nameplate capacity, with unbonded dry sand and 98% recyclability favoring iron and aluminum hardware volumes above 1,000 t/yr.

Lost foam casting lines cut pump and valve defect rates to 2-4% versus 8-15% for green sand, with ±0.25 mm tolerance and 6.3-12.5 μm Ra finish on 5-200 kg gray and ductile iron castings. EPC suits complex internal passageways but demands strict EPS density, refractory coating, and vibration compacti

For agricultural machinery parts weighing 20-200 kg in cast iron or aluminum, a lost foam casting line with EPS pre-expander + molding machine + sand system + line-frequency furnace delivers lower post-machining cost than green sand. Match line capacity to annual tonnage and pattern size before choo

Lost foam (EPC) casting suits aerospace buyers needing complex 1-500 kg iron or steel components at IT9-IT12 tolerance and Ra 3.2-12.5 μm finish, with ProCAST/JMatPro simulation recommended for gating design. Investment casting still wins for thin-wall superalloy aerospace parts; LFC is the right pi

Lost foam casting lines suit automotive iron and aluminum components from 0.5 kg to 500 kg, holding IT9-IT12 tolerances and Ra 3.2-12.5 μm as-cast. For an automotive line spec, lock down the material matrix, foam pattern accuracy, sand system, and downstream cooling first, then match equipment stage

For rail-component foundries, a static pressure molding machine is specified by flask size (commonly 800×600 mm to 1500×1200 mm), specific squeezing pressure (0.5-1.5 MPa), and cycle time, with 90-180 moulds/h typical for grey and ductile iron bogie, brake and housing castings.

Static pressure molding machines integrate air-flow pre-compaction with multi-piston compaction to reach mold hardness ≥85 and CT9-CT11 dimensional accuracy, with waste sand recovery above 90% in vortex regeneration systems. For energy equipment castings, they sit between 100+ molds/hour flaskless v

For electronics housings, static pressure molding machines must combine tight dimensional control, ESD-safe materials, and cleanroom compatibility. All-electric presses dominate this segment because they eliminate hydraulic oil contamination risk.

Static pressure molding machines are the right choice for lighting fixture housings with complex geometry, deep cavities, and uniform-density foam or resin requirements. Selection hinges on platen size, clamping force, sand/shot capacity, and whether the process is green-sand, resin-shell, or PU foa

Air-flow static pressure molding lines suit medium-to-large, high-finish castings at 50–120 molds/hr with uniform B-scale hardness of 85–90, while jolt-squeeze units still win for simple hardware. For hardware foundries, match machine class to casting size, output rate, and flask vs. flaskless layou

Static pressure molding machines are the right match for pump and valve foundries running 5-25 kg green-sand batches where high mold hardness, consistent flask density, and operator skill are available; high-pressure automatic lines suit high-volume cast iron valve bodies, while flaskless or jolt-sq

Static pressure molding machines for aerospace favor matched-metal dies, 1,000-3,000 ton clamp force, and 150-200°C platen heating for sheet molding compound (SMC) and fiber-reinforced phenolic/BMI composites. Selection hinges on platen size, heating uniformity, vacuum-assisted venting, and FST (Fla

For medium-to-large automotive castings, multi-piston static pressure molding lines delivering 85-90 B-scale mold hardness at 50-120 molds/hour are the spec-first choice, with flask vs. flaskless and PLC automation as the key decision forks.

For telecom enclosure molding, specify an automatic molding line that pairs UL 94 V-0 halogen-free compounds with IATF 16949-certified 1K/2K/insert processes, dielectric-stable resins (LCP/PPE/PPS), and ESD-compliant in-line automation for 5G and IoT housings.

For lighting-fixture housings, an automatic molding line is typically a two-shot co-injection or insert-molding cell running 0.5–1.5mm optical-grade PC/PMMA over ABS/PC-ABS, with 85–92% light transmission and ±0.05mm interface tolerance; tooling adds $5,000–$50,000 versus single-shot cells.

For hardware manufacturers selecting an automatic molding line in August 2026, the decision pivots on six hard specs, two mechanical platforms (DISA vertical vs SINTO horizontal), and three binding systems (green sand, resin PU, shell), with turnkey cells priced US$250,000–500,000 and cycle times sp

Automatic molding lines for pump and valve production should be selected around four binding constraints: family part weight (0.5-50 kg brass or stainless castings), shot size, clamp tonnage per cm² of projected area, and the downstream traceability step, where rotary-table laser marking at 2-12 s p

For agricultural machinery castings, a multi-piston automatic molding line running 50–120 molds per hour is the right pick when pattern height varies and mold hardness must stay at 85–90 B-scale; a Z1410-series jolt-squeeze machine remains the economical choice for small, high-volume simple parts. T

Aerospace-grade automatic molding lines for plastics run 200–1,200 ton clamping force with PEEK, PEI, PPSU, and PPS resins, holding ±0.02 mm tolerance and FAR 25.853 peak heat release ≤65 kW/m² at 2 min for cabin interior qualification.
Hot box core shooters from Quanzhou Sanjia and Goldsupplier peers list on Made-in-China with ISO 9001:2015 and CE marks; order prices typically run US$10,000-80,000 FOB and are driven by head count, shot weight and heated platen spec.
Degassing & refining unit selection for rail components hinges on melt volume, alloy family, and inclusion-control targets rather than rotor RPM alone. For aluminum rail transit castings, hydrogen should be driven below 0.15 ml/100 g and density index held at 3-4%, while total temperature drop acros

Automotive injection molding lines are sized around IMM clamp force of 500–3,000+ tf, robot payloads of 10–50 kg, and IATF 16949 process control. Selection balances part size, cosmetic class, resin behavior, and EOAT geometry against cycle rate and total tooling cost.

Sand mixers for rail-component foundries are selected on five engineering criteria: tonnage class, muller geometry, wheel loading, lining material, and binder-driven PLC recipe control. Continuous double-arm Durchlaufmischer units in the 15-30 t/h band are the default match for bogie-side and wheel-

Foundry sand mixers for energy equipment range from 1 t/h wheel mullers to 100 t/h continuous units, with planetary rotor models hitting 20-30 batches/hour at 30-75 kW. Selection pivots on binder system, throughput, and sand grain tolerance rather than price alone.

Sand mixer selection for telecom enclosures is dictated by thin-wall aluminium/sand moulding and tight dimensional tolerances; rotor-style units at 100-600 kg batch, 20-75 kW drive and 90-120 s cycles dominate the field.
Electronics-housing foundries should pick a sand mixer by binder chemistry first: high-shear rotor mixers (5-45 kW, 100-2000 kg batch) for phenolic/furan no-bake lines, continuous mullers (22-90 kW, 20-100 t/h) for greensand, and fast-batch paddle units for cold-box cores.
Lighting-fixture foundries should select rotor or double-arm continuous sand mixers sized 5-100 t/h with 22-75 kW main drives, matching binder chemistry to a 30-120 s mulling window before bench life expires. Skip drum mixers under 500 kg/batch for ferrous lighting hardware, and verify rotor tip spe
For hardware manufacturing foundries, planetary rotor sand mixers (10-50 t/h, 30-75 kW) suit high-precision iron and steel molds, while wheel-type mullers (1-20 t/h, 15-45 kW) fit small-batch green sand lines, and rotor/blade units (5-80 t/h) cover resin and sodium silicate systems. The selection pi
Agricultural sand-mix work on farms and equipment dealerships runs on 6-12 cu ft hydraulic-driven or towable mixers, 4-8 HP gas or 1/2-1.5 HP electric, paired to 3-5 min batch cycles and 36-64 bags/hour throughput.
Aerospace sand-mixer selection pivots on binder chemistry, energy density, and cleanliness, not brand: specify 10-15 kW per ton of compacted sand per hour, 1.5-2.5 m/s wheel tip speed, and closed dust-sealed charging for alumina-bearing aerospace alloys.

Sand mixers for automotive foundries pair batch capacity 100-1500 kg per cycle with sand/binder options that govern mould strength, gas evolution, and shake-out. Selection hinges on resin and sand type, throughput, and part mix.
Core making machines for energy equipment are specified around three binding decisions: process family (shell, hot-box, cold-box, or organic), moulding box size class, and cure throughput in shots/hour. Heavy-forging and transformer-core buyers now demand digital energy metering, LOTO-compliant guar
Core making machine selection for telecom enclosures depends on enclosure size, alloy, and production volume: shell processes suit thin-wall aluminum telecom cabinets under 200 kg, while hot-box and cold-box lines target cast-iron chambers and access lids for underground handholes. Buyers s
For electronic housings, choose a core making machine by binder chemistry first: shell or hot-box for thin-wall aluminum and zinc alloy enclosures (15–60 s cure, 230–280 °C box), cold-box phenolic urethane for tight-tolerance iron and steel EMI/RFI housings (TEA gas train, 20–80 cycles/h), and sodiu

Lighting-fixture foundries should match core-making machine type to casting weight and batch size: shell core shooters suit thin-wall lamp housings under 5 kg, while hot-box and cold-box lines serve heavier industrial luminaire bodies above 10 kg. Spec anchors include shot weight 3–40 kg, platen siz

Core making machines for agriculture machinery (housings, gearbox cases, plough shares, harvester concaves) are selected on part weight 1–80 kg, batch size 200–20,000/yr, and dimensional tolerance ±0.3 mm. Cold-box and shell processes dominate above 500/yr; for lower batches shell-core shooters with

Core Making Machine selection for aerospace components hinges on process temperature envelope, sand compatibility with reactive alloys, and shot intensity control. Shell and hot-box lines dominate titanium and nickel-superalloy tooling; cold-box and shell-core shooter setups fit higher-mix structura

For automotive hollow castings like engine blocks and water jacket housings, sand core making machine selection in 2026 turns on binder system, cure method, and cycle-time match to the casting line, with shell, hot-box, cold-box and CO2 process routes dominating. Engineers should match core geometry

Rail component molding lines in 2026 split into three families by feedstock: A36 steel cap-rail (1.27-2.14 lbs/ft, 19-20 ft stock), PC+ABS injection (sub-0.03 mm parting line), and powder-coated trim. Match the line to material, length tolerance, and takt before quoting.

For energy-equipment enclosures and busbar housings, an all-electric or servo-hydraulic molding line in the 50-300 ton clamp range (1.5-3.0 kWh/kg SEC) cuts specific energy 30-60% versus fixed-pump hydraulic presses. Match auxiliaries by heat-load math, not catalog price, to avoid the 6-8 week commi

For telecom enclosures, choose a molding line by enclosure size, structural-foam vs. injection decision, and required shot weight; structural foam molding suits large housings, while precision injection molding dominates sub-500 g telecom covers.

Hardware manufacturers selecting a molding line should match process type to part geometry, annual volume, and required tolerance. RIM fits large, low-stress housings at 0.4-0.6% shrinkage, plastic injection moulds in hardened tool steel run millions of cycles for fasteners, and overmolding bonds TP

Pump and valve foundries should choose molding lines by matching cast part geometry, alloy family, and required batch size: green-sand or shell molding for cast iron and steel valve bodies above DN50, automatic static-pressure molding for high-mix pump casings, and titanium or duplex parts increasin
For agricultural machinery castings and plastic components, pick a molding line by part size, hourly output, and surface-grade first, then match automation level. Multi-piston static-pressure lines deliver 50–120 molds/hr at 85–90 B-scale hardness for medium-to-large housings, while flaskless shoot-
Aerospace molding line selection in 2026 turns on three decisions: process family (injection, rotational, compression, LSR), resin system (PEEK, PEI, PPS, FKM, Nylon 12), and certification depth (AS9100, FAR 25.853, AMS). Match the process to part geometry, batch size, and traceability demand before
Automotive molding line selection hinges on matching shot weight, clamp tonnage, and IATF 16949 controls to part geometry: injection molding covers 30% of all plastic auto components at cycle times of 15-45 s, while 3D printing fills prototyping and low-volume EV niche runs.

Argon outperforms nitrogen for sensitive aluminum alloys, but nitrogen remains dominant in high-volume casthouses at 60% to 80% lower gas cost. For refinery vapor control, the 34,000 SCFM mobile thermal oxidizer class sets the scale for turnaround tank degassing. Selection hinges on alloy

Foundry degassing units (FDUs) for aluminium electronics housings target a Dichte Index of 3-4% and a hydrogen level below 2 ppm, with cycle temperature drops of 26-32°C. Inline rotary impeller degassers paired with refining flux tablets remain the dominant 2026 specification for thin-wall die-cast

Spec-first buyers pairing LED lighting fixtures with molten-aluminium fixtures and housings should select a degassing and refining unit by alloy, melt mass, and hydrogen tolerance, not by rotor brand. For typical 200-500 kg lighting-fixture casting batches, a 1.5-3.0 kW rotary degasser with 80-200 r

Rotary impeller degassing units cut hydrogen in molten aluminum from 0.30-0.50 cc/100g down to 0.08-0.15 cc/100g, with argon outperforming nitrogen on quality at 60-80% higher gas cost, making gas choice the central spec decision.
For pump and valve production, a degassing and refining unit is selected by matching alloy family, hydrogen target (≤2 ppm for alloy steel, Dichte Index 3–4% for aluminium) and the downstream casting process, with VD/VOD/RH/FDU as the four main equipment families.

Degassing and refining units for agricultural-machinery foundries are sized by melt mass, hydrogen target (Density Index 3-4%), and a 26-32°C temperature-drop budget during the refining cycle. The right FDU selection balances alloy family, ladle geometry, and rotor gas flow rather than nameplat

For aerospace aluminium components, degassing and refining units must hold hydrogen below ~2 ppm and Density Index within 3-4% to prevent microporosity in critical castings. Select rotor-stirred FDU designs sized to 26-32°C thermal budget, matched to alloy family and AMS specification.

Cupola furnaces suit foundries prioritizing low-capex iron melting (3–15 t/h) and coke-tolerant charge mixes; they are not fit where strict emissions limits, tight alloy chemistry, or high-purity steel dominate. For energy equipment buyers, the selection pivot is charge uniformity and energy balance

Cupola furnaces are continuous, vertical-shaft iron melters, not a fit for telecom-enclosure production: cast iron output and Fe-rich slag fail the ductility, weldability, and IP-rated surface needs of aluminum or steel cabinet bodies used at outdoor cell sites.

Cupola furnaces are vertical shaft melters historically used for grey and ductile iron, not for directly producing brass, copper, or tin lighting-fixture bodies. For authentic colonial lanterns and chandeliers, foundries should instead specify induction or crucible furnaces matched to the alloy, wit

A cupola furnace is a vertical shaft melting unit charged with alternating layers of iron, coke, and limestone; in 2026 it remains the lowest-cost bulk ferrous melter for sand-cast pump and valve bodies in the 1-20 t/h class.

Cupola furnaces are the most economical shaft furnace for small foundries, but they are generally unsuitable for aerospace component melting due to iron-carbon baseline melt, sulfur pickup, and limited temperature control. Aerospace buyers should spec induction or vacuum furnaces instead, reserving

Crucible furnace selection for rail components centres on matching furnace type to the alloy being melted, charge size, and rail-grade metallurgy. Induction crucible furnaces dominate ferrous rail-component melting because prefabricated crucibles with non-sintering backfill cut reline time, while sm

Crucible furnaces are not specified for telecom enclosure thermal management. Telecom cabinets use heat-treatment furnaces, induction heating, and resistance/convection systems, not crucibles for molten metal. When engineers need enclosure heating for bake-out, conformal-coat cure, or EMC gasket cur

Crucible furnaces for electronics housings are dominated by medium-frequency induction and vacuum-arc designs, with copper cold crucibles, graphite-clay-SiC refractories, and tilting tilt-pour configurations selected to keep melt chemistry clean below 1,800°C. For aluminium and magnesium housings, 6

Crucible furnace selection for hardware manufacturing hinges on matching furnace type (induction, gas, or resistance) to the metal being melted, batch size, and required melt cleanliness, with prefabricated crucibles in induction units cutting lining time dramatically versus in-situ ramming.

For pump and valve production, graphite-clay and silicon-carbide crucible furnaces with 1.5–3.0 kW medium-frequency induction ratings are the standard foundry pick, balancing 1200–1600°C melt temperatures for cast iron, bronze, and stainless trim. Selection hinges on melt capacity (50–500 kg), cruci

Select a 100–500 kg medium-frequency electric crucible furnace (rated 50–250 kW, 1–6 t/h melt rate) for agricultural-machinery iron casting. For copper/brass parts, pick a 50–150 kW unit, sized 50–200 kg.

Crucible furnaces for automotive parts foundries are typically specified as electric resistance or gas-fired tilting units in 100-500 kg capacity, with silicon-carbide or graphite crucibles rated 700-1200°C for aluminum, brass, and zinc-alloy melt decks. Selection centers on melt rate, alloy chemist

Holding furnace selection for rail components hinges on alloy family, throughput tonnage, and temperature uniformity (±5–10°C), with electric resistance and gas-fired units dominating 2026 OEM catalogs at US$113,000–450,000 per set.

Specifying a holding furnace for telecom enclosure die casting is unusual: enclosure castings are Al/Si alloys, so the unit must hold 660-720 °C melt with ±5 °C control, low bath depth for Stokes settling, and 100-2000 kg capacity to match cell cycle times, per.

Holding furnaces for electronics-housing die castings are typically 800-3000 kg electric resistance or gas-fired units, with 660-720°C aluminum melt held within ±5°C to feed high-pressure die casting machines. Selection hinges on temperature uniformity, inclusion control, and refractory choice rathe

Select a holding furnace for hardware manufacturing by matching alloy, temperature band, and process role to a specific heat source: vacuum induction for tight solidification control on aerospace-grade superalloys, gas- or oil-fired for larger iron/aluminum pours, and electric resistance holding onl

For pump and valve foundries producing bronze, cast iron, and aluminum bodies, a 5 to 40 ton gas-fired or electric holding furnace with ±5°C bath control is the typical spec gate. Selection hinges on alloy chemistry, melt-loss tolerance, refractory lining life, and takt-time matching to the casting

Selecting a holding furnace for aerospace components hinges on alloy chemistry, temperature uniformity, and trace-element control. For aluminum and magnesium alloys, electric resistance or gas-fired crucible designs dominate; titanium and nickel-superalloy work requires vacuum or controlled-atmosphe

For automotive parts foundries, holding furnace selection hinges on alloy family, shot size, temperature window, and energy source; electric resistance and channel-type induction dominate aluminum die-casting cells, while gas-fired reverberatory units remain common in iron foundries. Match furnace t

Gas-fired aluminum melting furnaces in the 1-10 metric tonne class are the workhorse for rail-component foundries, sized around 660°C melt point with refractory linings and regenerative burners for energy efficiency.

Gas-fired aluminum melting furnaces are still the workhorse of secondary aluminum plants, with reverberatory holding units typically sized 30-150 MT and regenerative-burner retrofits as the main efficiency lever. Selection pivots on charge size, melt rate, burner type, refractory class, and emission

For telecom-enclosure aluminum die casting, a gas-fired tilting melting furnace sized to 1-10 tonne capacity, paired with a separate holding furnace, is the standard match for enclosure alloys. Selection hinges on charge-to-cast ratio, SiC refractory grade, and combustion control per ATEX/IECEx zone

Gas-fired aluminum melting furnaces for pump and valve foundries should be selected on alloy family, melt rate, burner type and refractory class, with 660-760°C melt-zone and 700-1200 kg/h throughput bands as the dominant decision gates.

Gas-fired aluminum melting furnaces sized 0.5-10 t/h cover most agricultural-machinery foundry needs. Specify regenerative burners, 700-760°C bath, SiC refractory, and 35-45 m³/t gas consumption for 2026 capex decisions.

Line frequency induction furnaces for rail component melting are typically selected in the 500 kg to 40 t capacity band, with 2006/42/EC machinery compliance and 1600 deg C melt capability as the dominant commercial spec gates in 2026 sourcing catalogs.

For lighting-fixture aluminium and brass component foundries, the line frequency induction furnace (50/60 Hz mains-frequency coreless or channel type) is the correct pick over a 300–2500 Hz medium-frequency unit when melt mass exceeds roughly 500 kg per heat, holding duties dominate, and power infra

Line frequency induction furnaces for agricultural machinery foundries typically operate at 50/60 Hz mains frequency with capacities from 0.5 t to 40 t, drawing 1400 kW class power for steel-shell aluminum melting. Selection gates: 1) iron/steel vs aluminum melt path, 2) crucible lining chemistry, 3

Line frequency induction furnaces operate directly on 50/60 Hz mains, making them the right pick for high-tonnage, low-superheat aerospace melt batches. Aerospace work adds a thermal mass constraint: dense nickel and titanium alloys demand 1-3 t coreless or 3-15 t channel furnace capacity, with ramp

Line frequency induction furnaces operate directly off mains 50/60 Hz supply and are typically specified for cast iron and large ferrous melts, with capacities from 0.5 t to 30 t common in automotive foundry use. For automotive parts melting, selection hinges on melt mass, charge mix, holding duty c

For 2026 energy equipment builds, casting ladle selection turns on three gates: lining life vs. steel grade, 1100–1200°C preheat protocol, and compatibility with continuous casting or centrifugal turbine-bearing workflows. Match ladle type to melt mass and throughput before vendor selection.

Specifying a casting ladle for telecom enclosure production hinges on matching ladle capacity and refractory lining to the die casting alloy and batch size, with aluminum dominating the application due to thermal and weight advantages. Die cast aluminum supports tolerances of ±0.002 in and complex t

Casting ladle selection for lighting-fixture foundries hinges on matching pour-basin capacity, refractory lining class, and lifting geometry to small-batch aluminum and zinc pours typical of decorative luminaires. Specification gates cover 50-500 kg nominal capacity, hand-ladle or crane-ladle geomet

Hardware foundries selecting casting ladles in 2026 should match ladle capacity to 0.1–45 ton pour weights, with refractory lining and preheat discipline chosen per melt chemistry. Investment casting, permanent mold, and resin sand processes each impose different ladle geometry and pour-rate gates t

For pump and valve production, casting ladle selection hinges on three gates: alloy compatibility (special alloys vs carbon steel), batch size (1-piece prototyping vs 8,000 t/year foundries), and process route (investment, sand, or centrifugal casting). Top Chinese foundries pair ISO 9001 with PED-T

Aerospace casting ladle selection pivots on alloy family, pour temperature band, and Nadcap/AS9100 shop qualification rather than ladle volume alone. For titanium, nickel superalloy, and aluminum pours above 1500 °C, lined transfer ladles and pressurised bottom-pour systems dominate; for non-ferrous

For automotive part foundries, casting ladle selection hinges on melt capacity, refractory lining, and pouring metallurgy matched to iron, aluminum, or alloy steel pours. Match ladle class to part weight, alloy chemistry, and transfer temperature before any equipment quote.
Medium-frequency and IGBT induction melting furnaces dominate 2026 sourcing catalogs, with 100 kg to 40 t capacity ratings, 80 kW to 120 kVA power classes, and 2006/42/EC machinery-safety certification defining the entry spec for energy equipment buyers.
For electronics housings, specify medium-frequency coreless induction furnaces in the 100-500 kg melt-capacity class with vacuum or protective-atmosphere capability; they deliver the precise temperature control and clean melt needed for aluminum and zinc alloy die-casting. Selection must weigh melt

Coreless medium-frequency induction furnaces with 0.1-0.3 power factor and water-cooled copper coils suit brass, bronze, and aluminium alloy lighting fixture hardware, while lighting-grade induction lamp ballasts and driver housings draw on overlapping electromagnetic and thermal know-how. Specifier

For hardware manufacturing, pick induction furnaces by metal, melt mass, and frequency: coreless medium-frequency (1-100 t) for steel/iron, channel-type for bulk aluminum/copper holding, and vacuum units for reactive alloys. Verify OEM kW rating, water cooling, and inverter SCR spare-part supply bef

For pump and valve production, medium-frequency coreless induction furnaces in the 0.5-5 ton range with 250-3000 kW IGBT power supplies suit carbon/stainless steel casting; selection gates on melt mass, refractory, and cooling loop.
Agricultural machinery OEM specifiers should weigh medium-frequency (MF) coreless induction furnaces against channel types based on melt mass (under 1 t vs 100 t+), power supply stability, and duty cycle, since India market growth (USD 123.4M, 7.3% CAGR, 2026-2030) and global expansion to USD 3.91B
Vacuum and medium-frequency induction furnaces (10 kW–50,000 kW power range, 1 kg–70,000 kg capacity) are the dominant selections for aerospace component melting, with vacuum grades preferred for titanium and superalloys to limit gas pickup.

Induction furnace selection for automotive parts hinges on matching medium-frequency (1-20 kHz) coreless units to melt size, with 0.5-10 t capacity common for steel crankshafts and iron casting batches. Selection criteria include coil frequency, lining refractory, and power density for consistent me
Melting furnace selection hinges on metal family, charge form, and throughput. Induction, gas, and resistance furnaces each fit a different operating window. Use this 2026 spec map to match furnace type to your alloy, kWh budget, and melt-rate target before talking to suppliers.

For telecom enclosures, a medium-frequency induction melting furnace in the 250-2000 kg capacity class is the practical choice when batch-melting aluminum for die-cast or extrusion housings. Selection hinges on alloy, throughput, footprint, and enclosure IP rating, not on a single vendor spec sheet.

Aluminum die-cast electronics housings are best melted in medium-frequency coreless induction furnaces of 100–1000 kg capacity, with IGBT stacks for small batches and crucible furnaces for labs. Match furnace class to alloy, batch size, and EMC cleanliness, not just kW rating.

Lighting-fixture foundries cast brass, aluminum, and zinc alloy housings; selection pivots on melt capacity, alloy chemistry, and the temperature control accuracy needed for thin-wall LED heat sinks. The dominant choice for high-volume LED component production is a gas-fired or medium-frequency indu
Specifying a melting furnace for hardware manufacturing hinges on matching alloy, capacity, and power topology to the part. Mid-frequency induction dominates steel and iron melting; aluminum-shell and gas-fired crucible units cover non-ferrous hardware; arc and electron-beam units serve refractory a
Rail-component zinc die casting is dominated by hot-chamber machines in the 80T to 180T clamp range, with 25T to 40T cold-chamber units reserved for larger structural brackets. Selection pivots on shot weight, tonnage envelope, and certification (CE/ISO), not on brand alone.
Hot-chamber zinc die casting machines in the 20-160 ton clamp range with shot weights under 2 kg fit most energy-equipment housings, while cold-chamber units above 400 ton serve large inverter frames. Selection hinges on alloy, tonnage, shot weight, and thermal duty rather than headline price.

Zinc die casting machines for lighting fixtures are typically hot-chamber, 50-400 ton clamping force units, paired with Zamak 3 or Zamak 5 alloys for thin-wall housings, heat sinks, and decorative pendant bodies. Selection hinges on shot weight, platen size, surface finish grade, and post-process pl

Zinc die casting machines for hardware manufacturing are selected by clamping tonnage, shot weight, and Zamak alloy grade; current 2026 supplier offerings span 120-ton to 1650-ton HPDC platforms with part weights from 0.5 g to 50 kg.

Hot-chamber zinc die casting machines in the 16T to 180T clamp range fit most brass and zinc pump/valve bodies, with 25T to 38T units commonly specified for faucet-grade parts and gravity cells for sand-core plumbing fittings. Selection hinges on shot weight, plunger diameter, and die-closing force

Hot-chamber zinc die casting machines sized 50-800 tonnes suit agriculture-machinery housings and brackets under 500 g, with locking force, shot weight, and zinc-alloy Zamak 3/5/7 selection driving plant decisions.

For automotive zinc die casting, select a cold-chamber hot-chamber machine sized to part weight (under 1 oz to a few pounds), clamping tonnage from 80 to over 800 tons, and zinc-alloy grade that matches structural or cosmetic duty.

For energy equipment, choose a cold-chamber magnesium die casting machine in the 400T-9000T clamp range with 600-900 bar injection pressure and a real-time shot curve monitor; hot-chamber Mg machines do not exist and cold-chamber is the only credible answer.

Magnesium die casting for telecom enclosures pairs AZ91D/AZ31 alloy with cold-chamber machines in the 280T-800T clamp range, prioritizing thin-wall (1.5-2.5 mm), EMI shielding above 60 dB, and IATF 16949 / ISO 9001 audited supply.

For thin-wall electronics housings under 2 mm wall thickness and 0.6-1.2 kg shot weight, select a 400-1600 kN cold-chamber magnesium die casting machine with vacuum assist and 5-7 m/s intensification velocity. AZ91D and AM60B remain default alloys; AE44/AM50 grades push creep performance for hot-spo

Hot-chamber magnesium die casting machines in the 160-800 ton clamping force band suit LED heat-sink and luminaire housing production, with Mg density 1.8 g/cm3 and AZ91D/AM60B alloys dominating. Cold-chamber is reserved for larger structural castings, not thin-wall lighting parts.
Magnesium die casting machine selection for hardware plants centers on cold-chamber HPDC tonnage bands of 160-1600 tonnes, AZ91D and AM60B alloy compatibility above 400°C melt thresholds, and shot weight envelopes of 5-2500 g for auto, 3C, and power-tool parts.

Magnesium HPDC machines in the 400-5000 t clamping-force band are viable for pump and valve bodies where the 1.8 g/cm³ density advantage of Mg alloys offsets corrosion and reactivity limits. Spec the machine for hot-chamber (Mg) duty, servo-driven shot end, and vacuum/assist options; expect AZ91D, A

Magnesium die casting for aerospace demands HPDC machines of 800-5000 t clamping force with vacuum-assist, shot control under 2% porosity, and Mg-alloy-specific safety enclosures, with hot-chamber machines generally avoided for structural aerospace parts. Specifications, safety infrastructure, and O

Magnesium die casting machine selection for automotive parts hinges on tonnage class (typically 160-1600 t clamping force), hot-chamber versus cold-chamber architecture, and AM-series alloy readiness for thin-wall structural components at density 1.8 g/cm3.

Aluminum die casting machines for rail components are specified as cold-chamber units from Buhler, Frech, Ube, Italpresse, LK, Yizumi, Toshiba and Toyo, with 800-3500 ton clamping force, 0.5-3.5 mm wall targets, and EN 15085 / IATF 16949 weld-prep grade aluminum alloys as the dominant selection gate
Aluminum HPDC machines in the 350T-3050T clamping range dominate energy-equipment housing and heat-sink production, with IATF 16949 / ISO 9001:2015 supply now standard for grid and EV-adjacent buyers.

Aluminum HPDC machines in the 120-1650 ton clamping range cover most electronics-housing die casting; cold-chamber ADC12 and A380 dominate thin-wall EMI/RF enclosures over hot-chamber zinc and gravity processes.

Sandblasting equipment falls into three duty classes — mini, portable, and bulk — differentiated by pressure rating, abrasive media, and enclosure type, with China supplying the bulk of OEM units in 2026 at FOB tiers from US$1,000 small cabinets to US$57,999 large blast rooms.

Resin sand molding line installation requires a concrete foundation rated 1.5-2x equipment weight, ESD-grounded utility hookup, ISO 9001/CE compliance checks, and a documented commissioning cycle test before first pour. Use this guide to specify foundation, utilities, alignment, and acceptance crite

Aluminum extrusion profiles are classified into 6000-series alloys (6063, 6061, 6060) in T4/T5/T6 tempers, with 6063-T5 dominating architectural and 6061-T6 industrial use. Spec boundaries: thickness above 0.8 mm, width below 300 mm, surface options including anodized, powder-coat, electrophoresis,
Line-frequency (mains-frequency) induction furnaces split into coreless and channel-type designs, with the coreless variant dominating steel and iron melting and the channel (submerged-heel) type preferred for high-duty holding. The article maps variants, frequency bands, capacity ranges and selecti

Aluminum and zinc die casting dominate lighting-fixture housings, with 160-630 t cold-chamber machines standard for heat-sink bodies and 88-400 t hot-chamber units for thin-wall zinc trim. Match alloy, clamping tonnage, and shot weight to fixture type, not the reverse.

Shot sleeve selection for high-pressure die casting of automotive parts hinges on bore diameter, plunger tip match, thermal fatigue steel grade, and coolant geometry. For 2026 production lines, specify H13 hot-work tool steel with nitrided ID, water-cooled cavity, and a service life of roughly 80,00
For hardware manufacturing, a gravity die casting machine is selected by matching part weight, mold envelope, alloy family, and tilt/clamp envelope to the hardware's tolerance, surface, and annual volume targets. Typical GDC cells deliver up to 25 cycles/min, clamp 15-150 tonnes, accept 30 g to 80 k
Pump and valve producers should match gravity die casting machine selection to alloy (A356/A357/Cu-based), part weight 0.1-100 kg, ISO 8062 CT8 tolerance, and ≥3 mm wall thickness. Tilting GDC held 62.4% of 2025 type share; aluminum dominates automotive and machinery applications.
Gravity die casting machines for aerospace components in 2026 are typically specified at 9,000-20,000 kN clamping force with tilting geometry, paired with AlSi7, AlSi12, or magnesium alloys to meet tensile strength, elongation, and fatigue limits defined in NADCA Product Specification Standards.

For automotive parts weighing 0.5-30 kg, specify a tilting gravity die casting machine with servo-electric tilt (0.1 deg control), A380/ADC12 aluminum, and sand-core capability; high-pressure die casting remains dominant for high-volume thin-wall parts, while GDC wins on safety-critical aluminum str

Low pressure die casting (LPDC) machines operating at 0.3-1.5 bar typical fill pressure suit telecom aluminum enclosures where structural integrity, low porosity, and heat dissipation outweigh the throughput limits of the process versus HPDC. Selection hinges on shot chamber volume (200-700 cm3), ca

Low pressure die casting (LPDC) machines operating below 100 psi with 800-15,000-ton clamp force are increasingly specified for aluminum electronics housings, with vertical LPDC preferred for compact smartphone and data center thermal parts per 2025-2026 market data.

Low pressure die casting (LPDC) machines sized for lighting fixtures run on 0.3-1.5 bar fill pressure, 110-120°C mold temp, and 950°C melt hold, with steel dies and ceramic coating; selection hinges on platen size, shot weight, and alloy.
Low pressure die casting (LPDC) machines push molten aluminum or magnesium from a sealed furnace into a die at 0.20-1.00 bar, producing high-integrity wheels, engine blocks, and structural hardware. Selection for hardware manufacturing is dictated by alloy fluidity, mold temperature, clamping force,
For automotive wheels, knuckles, and cylinder heads, low-pressure die casting (LPDC) machines operating at 0.3–1.0 bar fill pressure with A356/AlSi7Mg0.3 alloy are the dominant specification, and the global LPDC machine market is valued at USD 2.25 billion in 2025 with a 6.0% CAGR to 2035.
For energy equipment housings, a vertical squeeze casting machine in the 650-2200 ton die-locking range, with direct squeeze pressure of 600-2000 kg/cm² and slow 0.5-2.0 m/s intake, fits aluminum and brass electrical enclosures better than high-speed die casting. Squeeze casting cuts porosity and ai

Squeeze casting machines in the 350-800 ton clamp range with vertical direct-gate presses are the dominant pick for telecom aluminum enclosures, delivering near-zero porosity housings that meet RF shielding and IP-rated sealing targets.
For electronics housings, vertical squeeze casting machines in the 160–1100 tonnage class (with 350 t as a documented pilot cell) deliver lower porosity, higher density, and T6 heat-treatable strength using AlSi7Mg, AlSi10Mg, ADC12, or A380 alloys. Selection hinges on tonnage match to projected area

For hardware manufacturing, squeeze casting machine selection hinges on matching 50-350 t clamping force, vertical/horizontal layout, and 0.5 m/s fill velocity to part geometry, alloy, and lot size.

Squeeze casting machines sized 500-1,500 tons clamp force with 3-5x intensification pressure fit agriculture-machinery housings and gearbox cases. Vertical 1,500-ton units (1,200-ton injection force) handle parts up to 0.84 m² projected area, suiting large tractor and combine castings. Compared with
Vacuum die casting machines for telecom enclosures should be specified by clamp tonnage, vacuum level (typically below 50 mbar), and shielding-gas capability, with die steel preheating and 5G-grade surface finish gating procurement. For 5G/mmWave filter housings, a closed-loop vacuum below 50 mbar w
Vacuum die casting machines in the 280-1300 kN clamping-force band are the practical spec window for thin-wall aluminum and zinc electronics housings, with 2026-08-05 supplier pricing clustered between $10,000 and $50,000 per unit on Alibaba.
Vacuum die casting machines for lighting fixtures use 50-2000 ton clamping force and vacuum levels below 50 mbar to produce porosity-free aluminum heat sinks and zinc LED housings, with selection driven by alloy, shot weight, and cycle time.

Vacuum die casting machines for hardware manufacturing typically run cold-chamber configurations from 280T to 1300T clamping force, with 80T-280T covering most bracket and housing work. For high-void hardware specify ≤50 mbar chamber vacuum; below 1 mbar is the threshold for aerospace-grade structur

Vacuum die casting machines cut dissolved-gas porosity in pump and valve bodies by holding cavity pressure below ~50 mbar during fill, with work vacuum typically 60-300 mbar and clamp forces from 800 kN to 9000 kN. Selection hinges on vacuum level, leak rate, alloy, and part wall-section rather than
Vacuum die casting machines for agricultural machinery production are selected on clamping force, vacuum level (typically 50-200 mbar absolute in die-cavity evacuation), and alloy compatibility. Match the machine class to part size and aluminum-silicon alloy grade before evaluating vacuum system int
Vacuum-assisted HPDC cells in the 350T-3050T clamp range dominate automotive structural-aluminum selection in 2026, with IATF 16949 suppliers pairing vacuum HPDC, FSW, and 5-axis CNC for leak-proof motor housings and liquid-cooling plates.

Cold chamber die casting machines are the standard pick for telecom enclosure production, where A380/A383 aluminum alloys exceed 4000 kN locking force requirements. Selection centers on shot weight, locking force, and shot sleeve diameter. Both new and used OEM equipment from Buhler, Idra, Frech, an

Cold chamber die casting is the go-to process for hardware-grade aluminum, magnesium, and copper alloys, with tonnage from 25T to 900T dominating 2026 hardware-plant procurement. Selection pivots on locking force, shot weight, platen size, and PLC architecture, with Chinese suppliers pricing 25T uni

Cold chamber die casting machines are the standard for aluminum, magnesium, and copper-alloy pump and valve bodies, with shot weights spanning roughly 0.05 lb (20 g) to 75 lb (34 kg) and section thicknesses of 0.02"–0.5" (0.5–12 mm). Selection for pump/valve work hinges on alloy, shot weight, clampi

Cold chamber die casting machines in the 800-1600 tonne clamp range are the default workhorses for aerospace structural castings in aluminum and magnesium, separating melt from injection to tolerate higher melt temperatures and reduce iron pickup. Selection hinges on clamp tonnage, shot weight, real

Cold chamber die casting machines (CCDCM) are the default choice for aluminum and copper automotive structural and powertrain castings above ~1 kg, with 700-ton models listed at USD 126,000-159,840 on B2B catalogs in 2026. Selection hinges on clamping tonnage, shot weight, and die-height envelope ma

For rail-component HPDC, shot sleeves are specified at bore ØD 80–150mm, length 400–1400mm, in nitrided H13 hot-work tool steel, with thermal regulation and tight 0.020" plunger-tip clearances.

Shot sleeve selection for electronics housings hinges on inner diameter 80–150 mm, hot-work tool steel with nitrided surface, and a closed-loop cooling ring to keep thin-wall die-cast enclosures dimensionally stable.
Shot sleeves are die-casting cold-chamber components, not lighting parts; specifying a sleeve for a luminaire requires translating cast-aluminum or cast-zinc hardware specs into fixture-grade finishes and UL/ETL/CSA wet- or dry-location ratings.
Hot-work tool steel shot sleeves sized 80-150 mm ID and 400-1400 mm length define the working envelope for pump and valve body HPDC tooling. Selection pivots on steel grade (H-13 to NADCA #207-90), thermal regulation, and lubrication routing.

Shot sleeve selection for agriculture-machinery die castings sits between the molten-metal feed system and the die, with bore diameter, length, wall thickness and lubrication set by shot weight and cycle time. Match sleeve material to alloy family, then verify against BS EN 16590-1:2014 safety-relat

Shot sleeves for aerospace die-cast components are selected on three hard data points: H13 tool-steel sleeves nitrided to 48–52 HRC, an inner-diameter/length envelope of Ø80–150 mm × 400–1400 mm, and a verified material stack-up per the OEM HTS data sheet. CuCrZr inserts cut thermal fatigue but rais
Hot chamber die casting machines in the 25-130 ton clamping range are the practical entry point for zinc and Zamak rail-component hardware, with FOB price bands between USD 25,000 and USD 52,800 per set on current supplier listings. Selection should prioritize shot weight, platen size, and tie-bar s
Hot chamber die casting machines (16-180 t clamp) are the right pick for zinc and lead alloy energy-equipment housings, fixtures, and small connectors when cycle time dominates the spec. For aluminum or magnesium power components, a cold chamber or vacuum machine is the correct class; hot chamber is

Hot chamber die casting machines in the 16-180 ton clamping-force band (HYBERS product line, 2026) suit Zamak-based pump and valve hardware, with selection driven by zinc-alloy melting point (~419°C) and shot-weight rather than tonnage. Match machine class to alloy family, projected shot weight, and

Hot chamber die casting machines suit agriculture-machinery zinc and Zamak parts under ~2 kg where short cycle, low melt loss, and minimal floor footprint drive ROI; cold chamber units become mandatory once aluminum or magnesium alloys enter the spec, and tonnage, shot weight, platen size, and shot
Hot chamber die casting machines dominate zinc and magnesium automotive trim production, with 20-300 ton clamp tonnages and US$24,640-54,000 price points on the 2026 China export market. Selection hinges on alloy chemistry, shot weight, and cycle time; cold chamber remains mandatory above ~1% magnes
Energy-equipment die castings — EV inverter housings, PV inverter heat sinks, wind-pitch housings — sit in the 160-1300 t cold-chamber range and drive selection around alloy, tonnage, and shot weight, not price. Use this spec map to match machine class to part geometry.

For electronics housings, a 160-400 ton hot- or cold-chamber die casting machine running zinc or aluminum alloys is the most specified platform in 2026, with cycle times under 60 s for thin-wall enclosures.

Hardware buyers sourcing die castings should pick the machine class by alloy, tonnage, and IATF 16949 evidence, with Chinese factories offering 25-1650 ton HPDC, hot-chamber 25-80 ton zinc units, and gravity dies up to 50 kg part weight as the practical 2026 shortlist.

For pump and valve bodies, cold-chamber die casting in the 400-5000 t clamping-force range suits aluminum and brass alloys, while hot-chamber machines cover zinc and magnesium components under 1 kg. Match shot weight, plunger diameter, and intensification ratio to the part's projected area, wall thi

Die casting machines for agricultural machinery are typically 800-1600 t cold-chamber aluminum units, paired with 150-400 t hot-chamber zinc cells for thin-wall housings, with selection driven by clamping force, shot weight, and alloy.
Aerospace die casting is dominated by cold-chamber machines sized 350-1300 tonnes, with vacuum-assist and magnesium variants on the near-term sourcing list.
Automotive die casting cell selection hinges on alloy family (Al vs Zn vs Mg), clamp tonnage band (80T-3050T), and shot type (hot-chamber vs cold-chamber). Cold-chamber HPDC dominates structural aluminum body and EV parts; hot-chamber suits zinc under 80T for thin-wall trim and hardware.

Indian and Chinese industrial oven and furnace manufacturers dominate the SME sourcing map in mid-2026, with listed ex-works prices from Rs. 85,000 to Rs. 2,00,000 in India and US$1,500-8,000 on Made-in-China for hot-air drying ovens spanning 200-500°C.
Industrial ovens divide into batch, conveyor (belt/roller), tunnel, vacuum, and infrared/UV categories, each matched to a specific temperature range, atmosphere, and throughput profile. Selection hinges on max temperature, ±°C uniformity, atmosphere control, and production cadence rather than brand.

China hosts 2,000+ sandblasting equipment manufacturers and Alibaba lists 1,246 cabinet suppliers, with sandblasting machine price bands from US$2,500 to US$52,000 per set. India remains a secondary sourcing cluster.
Sandblasting equipment selection hinges on matching nozzle pressure (typically 80-150 psi for gravity-feed pots, up to 150 psi for siphon), abrasive compatibility, and dust-control duty. Pick pressure-blast for heavy rust/paint, siphon for light profiling, and wet/vacuum systems for silica-restricte
Forging press selection splits along three machine classes — mechanical, hydraulic, and screw — each pairing distinct force, stroke, and energy characteristics with specific part geometries, from 7,500 kN hot-formers to 50,000-ton hydraulic giants.
Investment casting equipment spans wax injectors, shell-building lines, dewaxing autoclaves, and metal-melt furnaces, with selection driven by part weight, alloy, and tolerance band. Match equipment class to the part envelope, alloy pour temperature above 1000 °C, and required CT tolerance grade bef

Investment casting equipment selection hinges on matching wax-injection pressure, shell-line capacity, and smelting furnace type to alloy and tolerance. C-type hydraulic wax injectors, double-site hydraulic injectors, and pneumatic machines cover different throughput bands; induction melting furnace
Cast aluminum alloy selection is governed by tonnage, shot weight, and alloy family — 80T–400T cold-chamber machines dominate aluminum work, with 2026 China spot pricing from US$48,000 to US$80,000 per unit. Hot-chamber units below 38T handle zinc and lead at US$10,000–US$22,000, while aluminum allo
Cast aluminum alloys split into gravity-cast and high-pressure die-cast families, with A356/A319 dominating sand/gravity work and A380/A383 covering most HPDC housings. Selection hinges on Si, Cu, and Mg content versus strength, ductility, and pressure tightness.

Pick cast aluminum by matching the alloy family to duty: 3xx.x (Al-Si) for thin-wall/high-pressure die casting, 4xx.x for sand/permanent mold, 2xx.x for elevated-temperature strength, 5xx.x for marine corrosion resistance, and 7xx.x for high-strength structural shells. Confirm casting process, heat

China-based aluminum coil suppliers dominate global B2B sourcing in 2026, with continuous-cast 1100 coils, prepainted 3xxx/3003 coils, and PVDF-coated stock available at 0.2-4mm thickness by 800-1900mm width and 10000 m.t./month line capacity.
Aluminum coil is a rolled flat-rolled aluminum product supplied in gauges 0.10-4.0 mm and widths 10-2000 mm across alloys AA1050 through AA8011, used in construction, HVAC, packaging, and transport. Selection hinges on alloy series, temper (H/O/F), coating, and end-use form factor.
Choosing an aluminum coil comes down to matching alloy series to duty: AA1100 for formability and ceilings, AA3004/AA5xxx for marine/structural corrosion resistance, AA8079 for packaging. Spec thickness 0.2-12 mm, width 10-2500 mm, verify CE/ISO9001/SONCAP per EU construction and channel-letter PE b

China remains the dominant aluminum sheet supply base, with HC Aluminum alone listing 300,000 t/yr capacity and Okorder advertising 10,000 t/month per RFQ; 1000/3000/5000/6000 series coil, plate, and checker plate dominate B2B catalogs at typical 0.3-6 mm gauges.

Aluminum sheet is classified by alloy series (1xxx-7xxx) and thickness bands (sheet 0.15-6.0 mm, plate 6-200 mm), with 3xxx, 5xxx, and 6xxx grades dominating automotive, marine, and architectural uses. PE-coated color sheets at 16-25 micron paint and 4x8 ft panels are the stock format for building f

Aluminum sheet selection hinges on alloy series (1xxx/3xxx/5xxx/6xxx), temper (O/H32/T6), thickness band (0.15-6.0 mm sheet vs 6-200 mm plate), and end-use duty. Match Mg2Si-rich 6061-T6 for structural frames; 5052-H32 for marine/chemical tanks; 3003 for forming; 1100 for chemical/packaging.
Aluminum extrusion profile and an aluminum die casting machine serve different production roles: extrusion forces heated billet through a die to make constant-cross-section profiles 3–13 m long, while die casting injects molten aluminum into a closed steel mold at 800–950 °C to form complex 3D parts
Choose aluminum extrusion profiles by matching alloy-temper (6063-T5/T6, 6061-T6, 6082-T6) to duty: 6063-T5 for architecture, 6061-T6 for structural, 6082-T6 for high-load. Verify GB/T 5237 surface finish, PA66GF25 thermal-break, ISO9001 certification, and T-slot dimensional standards before procure
Magnesium die casting suppliers are concentrated in China, with 100+ vendors on Alibaba and made-in-china.com offering hot-chamber HPDC for AZ91, AM60, and AM50 alloys at MOQs from 1 piece. Buyers should match alloy, machine class, and IATF 16949 certification to the application before sourcing.
Magnesium die casting spans hot-chamber, cold-chamber, and thixomolding routes using AZ91, AM, and creep-resistant rare-earth alloys at 1.8 g/cm³ density, serving automotive, electronics, and aerospace components. Selection hinges on volume, temperature load, and corrosion class rather than generic
Zinc die casting uses hot-chamber machines in the 16-180 tonne clamp range and suits Zamak alloys for thin-wall, high-volume parts, while general die casting machines cover both hot-chamber zinc/lead work and cold-chamber aluminum at 25-280 tonnes. Pick the technology by alloy melting point, part ge

Zinc die casting suppliers cluster heavily in China's Zhejiang, Shandong and Guangdong provinces, with verified trading-platform directories listing 557+ zinc-die-cast-mould SKUs and 1,282+ zinc-casting factories. The global sourcing map for 2026 spans China (bulk OEM/ODM), India (precision automoti

Zinc die casting covers hot-chamber HPDC on Zamak-type alloys, with part weights from under 1 g to several pounds, serving automotive, hardware, electronics, and medical sectors. Three process routes — hot-chamber HPDC, gravity, and miniature — dominate procurement decisions in 2026.
Zinc die casting suits thin-wall, high-tolerance parts under 25 mm wall with 0.1 mm machining stock, using ZAMAC 3/5 or ZA-8 alloys. Use hot-chamber machines, watch tooling $15K–$150K, and pick suppliers with ISO 9001:2015 audits.

Aluminum die casting and die casting machines are distinct procurement objects: the former is a part or service (typical 2026 China export pricing US$0.50-$2.89/piece for housings and covers), the latter is the capital equipment (2026 China FOB ranges roughly US$10,000-$50,000 per set). Buyers shoul

Aluminum die casting suppliers cluster heavily in China's Jiangsu, Zhejiang, Shandong and Hebei provinces, with ISO 9001 and IATF 16949 cited as the dominant certifications and ADC12/A380 as the most quoted alloys. Sourcing on Made-in-China, Okorder and manufacturer-direct channels in 2026 surfaces
Aluminum die casting splits into high-pressure cold chamber, hot chamber (limited use), gravity, low-pressure, and vacuum variants, with high-pressure dominating ~95% of structural aluminum parts. Selection hinges on alloy (A380, A383, A384, ADC12), tonnage (250-850 ton), and required surface integr

Aluminum die casting selection in 2026 hinges on matching the die-casting machine, alloy grade, and post-process chain to the part's geometry and duty. Cold-chamber units dominate for aluminum; one-stop China suppliers like Bian Diecast cover mold design, casting, CNC machining, and finishing under

Low-pressure die casting (LPDC) machines fill molten metal into dies at 0.02-0.1 MPa from a sealed furnace below, with tonnage bands from 25T mini units to 280T industrial lines. The process targets aluminum alloys A360, A380, ADC10, ADC12, ZL102 and ZL104, making it suited to wheels, oil tanks and

Gravity die casting machines fill the gap between sand casting and high-pressure die casting, with 2026 sourcing data showing PLC-controlled units handling brass, zinc, and aluminum alloys across automotive, hardware, and machinery sectors.

Hot chamber die casting machines serve low-melting alloys (Zn, Mg, leaded brass) with 25-900 ton clamping force, sub-1s cycles for sub-ounce parts, and contrast with cold chamber units above 650T.

A cold chamber die casting machine melts aluminum, magnesium, or copper alloys in a separate furnace and injects them into a closed die with a horizontal shot cylinder, suiting high-melting-point alloys and large structural parts in automotive and 3C industries.

A mold base's 5-year total cost of ownership is dominated by steel grade, machining complexity, tryout scrap, and downtime risk — purchase price is typically 35-55% of lifetime cost. Model selection by hardness, cavity count, and delivery lead time is the highest-leverage spec decision a tooling buy

Mold base installation hinges on five binding checks: platen flatness within 0.03 mm across 1000 mm span, leader-pin/R-bushing clearance at 0.02-0.04 mm, clamp-foot torque to 35-45 Nm on M16 class 8.8 bolts, and guided ejection reset. Skip any one and parting-line flash or guide-pillar galling follo
Mold bases divide into four working classes by steel grade, hardness range, and shot count: LME-standard 50-series (P20/S50C, 28-32 HRC, ≤500k shots), through-hardened H13/718 (HRC 38-44, 0.5-1M shots), stainless 420/2083 (HRC 30-36, corrosive polymers), and beryllium-copper inserts (>50 W/m·K therm
Sand casting mold TCO is dominated by use-phase energy, sand reclamation, and pattern maintenance, while the price tag covers under 10% of lifetime spend. The largest savings levers in 2026 are pattern life, reclamation yield, and defect-driven scrap.

Sand casting mold installation centers on flask alignment, parting-line sealing, and proper sand compaction (green-sand at 30-40% clay moisture, rammed to ~70-80 AFS density index). Hand floor operations suit runs below ~200 molds/shift; flaskless horizontal molding lines like the 600x700 to 1000x10

Green-sand, resin-bonded (no-bake / shell), lost-foam, and 3D-printed binder-jetted sand molds are the four classifications engineers spec against, with green-sand dominating ferrous volume and 3D-printed molds unlocking lattice and under-cut geometry that traditional sand cannot match.
Die casting die total cost of ownership spans die steel, machining, tryout, perishable wear components, cycle-time-driven energy, and end-of-life scrap — with the die itself typically 30–60% of multi-year TCO. Buy decisions on a quoted die price alone routinely underestimate lifetime cost by 2–4×.
Die casting die installation on a 280-800 ton high-pressure machine follows a defined sequence: die lift, platen alignment, clamp-force verification, and coolant/electrical hookup before the first shot. NADCA-aligned shops cite CT8 linear tolerance from ISO 8062 as the post-installation acceptance b
Heat treatment furnace TCO over a 15-20 year service life is dominated by energy, refractory maintenance, and atmosphere gas consumption, not the purchase price. Buy-side focus belongs on kWh/kg, insulation class, and atmosphere control architecture, with vacuum, atmosphere, and aluminum furnace cla

A heat treatment furnace delivers uniform, controllable thermal cycles for annealing, quenching, and solution heat treating between roughly 150°C and 1,200°C, with aerospace builds reaching ±3°C uniformity, but costs, atmosphere control, and quench logistics decide fit.

Heat treatment furnace installation hinges on matching chamber size, maximum temperature, and atmosphere class to the workpiece, then verifying clearances, ventilation, and utility drops before commissioning. Lab chamber units run 1000-1300 °C at 5-65 L; industrial gas or vacuum lines span US$1,200-
A riser cutting machine's total cost of ownership is dominated by energy and maintenance, with acquisition typically below 30% of lifecycle cost over a 10-year horizon. Specifying VFD-driven spindle drives, servo rather than hydraulic clamping, and ISO 9001:2015-certified consumables cuts TCO materi

A riser cutting machine is a foundry-specific cutting machine engineered to shear off feeder heads and gate stubs from castings, delivering high cut quality on steel, iron, and non-ferrous parts but requiring matched clamping force, abrasive consumables, and operator guarding. Select a hydraulic or
Vertical band-saw riser cutting machines (e.g., Multicut VBM-150) anchor a 3-step install: anchor/level the 550 kg frame, route 3 HP + 0.14 HP coolant power with coolant flood set, then verify blade tracking and tension before first cut.

Riser cutting machines are classified by cutting technology, automation level, and riser diameter capacity, with pneumatic, hydraulic, and CNC servo platforms dominating foundry shops. Selection hinges on riser neck diameter range, cut-off wheel speed, and clamping force relative to sprue hardness.
Fettling grinder TCO hinges on wheel consumption, abrasive spec, and dust extraction downtime: a 5–9 kW pneumatic or electric unit running two shifts typically lands its 5-year cost at 3–5× purchase price, dominated by consumables and labor.
Fettling grinders deliver high metal-removal rates on castings (12-24 inch wheels, 3-15 HP motors) but trade off operator safety, vibration exposure, and dust load for raw productivity.
A fettling grinder installation is governed by three hard gates — wheel speed matching, guarding integrity, and extraction airflow — that decide whether the unit passes first-start commissioning on a foundry floor.
Sand blasting machines deliver low-cost, flexible abrasive surface finishing across US$900–2,200 portable units up to industrial rooms, but dust exposure, media consumption, and operator-skill demands limit them versus enclosed shot blasting systems.

Sand blasting machines split into suction-feed, pressure-feed, wet, and cabinet configurations, plus wheel-blast variants for plate and pipe — selection hinges on workpiece geometry, abrasive media, and dust-control class. Atlas Copco frames the process as abrasive particle propulsion at high veloci
Vibratory fluid-bed sand coolers cut reclaimed foundry sand to 1.6–2.2% moisture at ±0.3% tolerance and below 49°C outlet, but cap single-unit throughput around 40–100 TPH and carry 15–30% higher capex than wet-belt or rotary alternatives.

A shakeout machine separates castings from sand molds via vibration or rotary impact, cutting decoring labor 60-80% versus manual hammer-out, but adds capital cost, noise 85-110 dB(A), and dust-load on downstream dedusting. Spec it when batch volume justifies the payback band.
Shakeout machines separate castings from molding sand on a perforated or grizzly deck and are classified by drive layout (above-deck vs below-deck), vibration mode, and casting-application family. Foundries typically choose among vibratory, rotary drum, and barrel-horse designs sized to a 5:1–60:1 s
A sand reclamation unit recovers used foundry sand back to reusable bond strength through thermal or mechanical processing, cutting virgin silica intake and landfill cost, but only if the feed is bonded with thermally-degradable resins and the plant can justify its 200-600 kW power draw.

A casting mold install must reconcile the mold type (sand, shell, permanent, high-pressure die) with the mounting surface, parting line, ejection stroke, and cooling circuit before the first pour. Spec-driven acceptance values (draft angle ≥1–3°, parting-line flash ≤0.5 mm, cooling line pressure tes
Casting mold types are classified by both process family (sand, die, investment, centrifugal, plaster, continuous) and production-volume tier, with SPI Class 1-5 mapping tool life from over 1,000,000 cycles down to 500 prototype cycles.
Shot blasting machine TCO runs 3-5x the purchase price over a 10-year service life, driven by abrasive media, wear parts, energy, and dust-collection compliance. This article maps the cost stack, ranks driver impact, and gives a selection matrix for buyers.
Shot blasting machines use high-velocity abrasive impellers to clean, descale, and profile steel surfaces, delivering faster throughput and lower per-ton abrasive cost than manual or sand-blasting alternatives in heavy-industry settings. Trade-offs include high capex, abrasive dust management overhe
Shot blasting machine installation demands a fixed sequence: site prep with dust-collector ducting, foundation anchoring, blast wheel alignment, abrasive-circuit commissioning, and Almen arc verification. Q-series models like Q37, Q35, Q69 follow standard hook/table/roller-conveyor layouts per OEM d

Shot blasting machines split into nine functional families: tumble belt, rotary drum, hook, overhead conveyor, roller conveyor, rotating table, crawler, manual ID lance, and air/peening cabinet. Selection turns on part geometry, batch size, and in-line vs standalone use, with centrifugal wheels domi

Shell core machine total cost of ownership runs 3-5x the purchase price over a 10-year life, driven by energy, resin/binder, sand, wear parts, and unplanned downtime. Engineering-led TCO models built for injection moulding and vacuum equipment translate directly to foundry coring, where dynamic trac
Shell core machines are classified by station count (single vs dual), heating medium (gas-fired vs electric), core box split orientation (vertical vs horizontal), and automation level, with sand blow capacities typically ranging from 5 L to 75 L per cycle. Harrison single-station models span 10–24 i

Shell core shooter total cost of ownership is dominated by resin and binder, amine gas, and 7-15 year tooling/service life, with energy and downtime swinging the bill by 10-25%. Buy on lifecycle, not sticker.

A shell core shooter is a sand-core-making machine that uses sudden expansion of compressed air to propel resin-bonded core sand into a heated core box, where it cures into a rigid sand core. It suits medium-to-high volume foundries needing tight dimensional control and short cycle times, but it tra

Shell core shooters divide into two main types — top-blow and rollover (swing-door) — both using the Croning resin-sand process at 200-260°C, with sub-classes by automation, plate size, and cure mode. Foundries select by core weight, cycle time, and parting line geometry; cold-box systems remain a s

A hot box core shooter's 15-20 year total cost of ownership is driven less by machine price than by gas or electric die-heating energy, resin binder consumption, and tool wear. Lifecycle spend is dominated by thermal energy and consumables, not capex.

Hot box core shooters deliver fast cycle times and high core density for resin-coated sand, but trade off against tooling heat-up energy, fume management, and limited core geometry. The sweet spot is short-run, thin-walled, high-precision cores where the per-shot economics and surface finish outweig

Hot box core shooters cure resin-coated sand cores at 200-260°C inside heated core boxes and split into vertical-parting and horizontal-parting machines by mold opening direction. Vertical types cover 20-100 kg cores, horizontal types reach 120 kg, with 100-set/month export supply from China-based O

Cold Box Core Shooter TCO spans a 15-20 year lifecycle, with amine gas, resin, sand, amine scrubber maintenance, and PLC retrofit typically outweighing the 2-5x purchase price gap between manual and rotary units.

Cold box core shooters use amine-cured phenolic binder and pneumatic sand shooting to produce high-strength, complex sand cores at scale. Advantages include high dimensional accuracy, fast cycle, and low amine emissions on modern gassing systems; drawbacks cover capital cost, amine handling, and too

Cold box core shooters are classified by curing chemistry, parting-line orientation, station count, and sand capacity. The four dominant variants are amine-cured, CO2-cured, vertical-parted, and horizontal-parted shooters, ranging from 3.2 kg single-station units to multi-station rotary machines.

V-Process vacuum molding uses dry sand sealed with heated EVA film and atmospheric pressure differential, achieving a reported 95% sand recovery rate, low dust, and tight dimensional accuracy. Trade-offs include film cost, vacuum-system dependency, and limited suitability for certain high-temperatur

V-Process vacuum molding lines use heated EVA film and dry sand under ~0.06-0.08 MPa vacuum to form binderless molds with a stated 95% sand reclamation rate. Installation centers on vacuum stability, dry-sand logistics, and film-sealing quality rather than chemical binder handling. This guide maps s

V-process (vacuum) molding lines use dry sand held by atmospheric pressure on EVA film, with a 95% sand reclamation rate, flask sizes up to 1600x1250x400 mm, and throughput of 6-10 molds/hour on HWS VDT-6 class plants. The technology was patented by Japan's Sinto Group in 1971 and is now licensed to
Resin sand molding lines deliver high dimensional accuracy and complex-casting capability for batch production, but trade off against higher resin cost, amine gas emissions, and intensive sand reclamation. Best suited to medium-to-large iron and steel foundries running medium-to-high volume runs of
Shell molding machine TCO is dominated by energy, resin-binder sand, and pattern wear, not by the 5-15 percent share visible in the acquisition line item. Lifecycle math over 10-15 years typically lifts energy and maintenance to 50-70 percent of lifetime cost.
Shell molding machines deliver near-net-shape resin-shell sand molds with ±0.2-0.5 mm dimensional tolerance and superior surface finish, but trade off against 6-10× higher per-mold tooling cost, longer cycle times, and limited suitability for very high-run ferrous castings versus green-sand or autom

Shell molding machine installation is a 5-7 day field procedure covering foundation, leveling to 0.05 mm/m, utility hookup (LPG or electric, 5-6 bar air, 380 V 3-phase), and cycle acceptance at 40-70 s per shell. Use this spec map to plan the install and reject units that fail the pressure or flatne

A lost foam casting line installs in three staged zones — white-area foam-pattern production, yellow-area coating/drying, and black-area sand-mold/pouring — and acceptance hinges on dry-sand compaction under negative pressure. Capacity is custom-built in 3,000 t or 5,000 t/yr modules with floor spac
Lost foam casting lines (LFC) are evaporative-pattern production systems classified by automation tier (manual / semi-automatic / full-automatic), alloy range (ferrous vs non-ferrous), and part size class, with typical turnkey capacities of 3,000–5,000 t/yr and three process zones — white (pattern),

Static pressure molding machine TCO is dominated by 5-10 year lifecycle costs—energy, sand media, wear parts, and downtime—beyond the 24-300 kW unit price. Buyers who model only Capex typically underestimate total spend by 30-50%.

Static pressure molding machines deliver high-density green sand molds with uniform hardness of 85–95 and 2–5× the compaction force of squeeze or jolt methods, suiting medium-to-large ferrous cast runs. Trade-offs include 15–25% higher capex than jolt-squeeze lines, longer pattern-change cycles, and
Static pressure molding machine installation is governed by JB/T 12241-2015 for model coding, basic parameters, and acceptance testing in China. The standard defines the equipment, compaction ratio, and test methods, with 1-ton MOQ China-built units priced near US$1,200–1,500.
Automatic molding line total cost of ownership over a 10-year horizon is dominated by energy, maintenance, and downtime losses, with capital cost typically 25-35% of the stack. The Springer dynamic TCO framework treats energy and maintenance as variables that cannot be solved statically. Buyers
An automatic molding line delivers 3-5x throughput over manual flask handling and cuts per-mold labor to roughly 0.05-0.15 FTE, but capex sits in the USD 250k-2M band and requires 2-6 months commissioning before stable output is achieved.

Automatic molding lines are classified by molding medium — green sand, resin sand (including DISA), shell, static-pressure, and PU foam — with selection driven by part weight, dimensional tolerance, and annual throughput up to 10,000+ tons.
Sand mixer TCO over a 10-15 year service life is driven 60-75% by energy, wear parts, and downtime — not the purchase price. This article breaks down the cost stack, ranks the main mixer types, and surfaces the spec levers that move lifecycle cost.
Foundry sand mixers fall into four working classes — clay/green, resin (furan/phenolic), coated (hot/thermal), and self-hardening — selected by binder chemistry, throughput (t/h), and sand-to-binder ratio. Vertical rotor-wheel and horizontal twin-shaft paddles are the two dominant agitating geometri
A core making machine's 10-year total cost of ownership is dominated by energy, sand/resin consumables, and maintenance—not the purchase price. Below is a driver-by-driver breakdown of where the money actually goes for foundries.

Foundry core making machines split into shell process, hot-box, cold-box, and coding (shoot & squeeze) classes, each matched to a binder chemistry, cure cycle, and production volume. Selection is driven by sand-binder compatibility, dimensional tolerance, and required cycle time per core.

Molding lines fall into four process families — injection, blow, compression/sand-shell-static pressure, and casting/depositor — with five SPI mold classes (101–105) defining injection-mold build grades. Selection is driven by material, annual volume, tolerance, surface finish, and cycle, not by a s

A degassing & refining unit's 20-year total cost of ownership is driven 60-80% by energy, consumable refractories, and process-gas use rather than the purchase price; aluminum foundries and die-casters that model these operating lines typically recover 14-30 months of payback on rotary versus static

A degassing and refining unit strips dissolved hydrogen and inclusions from molten aluminum alloys, with rotary impeller degassers holding bath at 720-760 °C delivering hydrogen drop from ~0.30 to under 0.10 ml/100 g Al and inclusion removal above 70 percent. Trade-offs include flux consumption, ref

Aluminium-foundry degassing & refining units are installed in a fixed sequence — furnace-tap launder, rotary injector, melt treatment box, gas-supply skid, then baghouse — with argon purge, refractory pre-heat, and lance immersion depth verified before first pour. Treatment times of 8-20 min, hydrog

Foundry Degassing Units (FDU) for aluminum melts are classified by gas-injection method — lance, rotary impeller, porous plug, and flux-tablet — with hydrogen control verified by Density Index targets of 3-4% and a measured 26-32 °C melt-temperature drop over the refining cycle at industrial sites.

Cupola furnaces are vertical, cylindrical shaft melters that dominate grey iron foundries thanks to low fuel cost and high melt rate, but the same geometry forces operators to accept batch tapping, limited steel melting, and significant stack emissions. Use a cupola only when continuous grey or duct
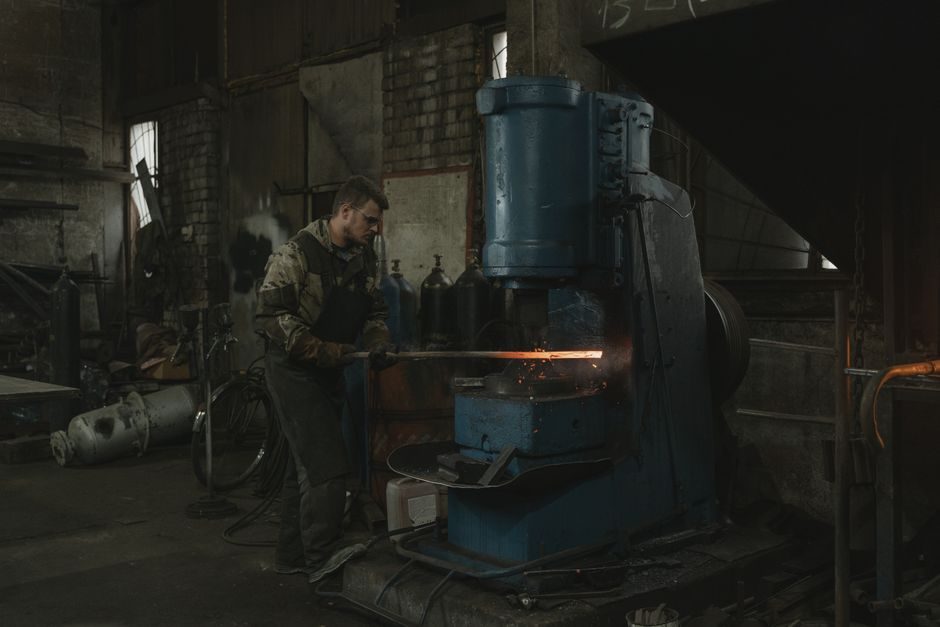
A cupola furnace is a vertical, cylindrical, air-blown coke-fired shaft furnace used to remelt cast iron for foundry pouring, with the four working classifications being cold-blast, hot-blast, water-cooled (basic-lined), and dual-shell variants. Selection hinges on melt rate (TPD), tuyere count, lin

Crucible furnace installation hinges on foundation design, refractory curing, stack drafting, and power or fuel train safety; concrete slab thickness 100-150 mm, refractory dry-out 24-72 h, and stack draft 10-30 Pa are typical acceptance benchmarks across small foundry and laboratory builds.
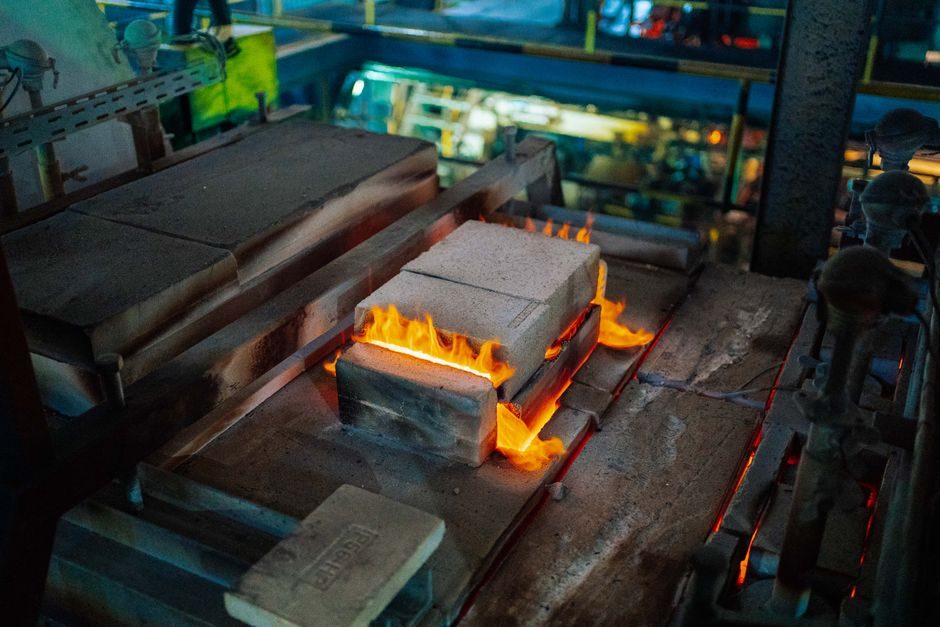
Crucible furnaces are melting units that heat a removable crucible from the outside, classified by heat source into induction, fuel-fired, and resistance-electric types. Selection hinges on melt capacity, alloy reactivity, and shop power availability; the crucible induction furnace remains the domin
A holding furnace is a refractory-lined vessel that keeps molten metal at pouring temperature between melting and casting, with key advantages of energy savings, alloy homogeneity, and continuous casting supply, and disadvantages of refractory wear, dross generation, and idle-heat loss. Selection de

A holding furnace is a refractory-lined vessel that maintains molten metal at a controlled temperature between melting and casting, with main types including crucible, induction, and reverberatory designs selected by alloy, capacity, and temperature stability needs.
A gas-fired aluminum melting furnace delivers high BTU density and faster charge melt than electric resistance or induction units, but trades off NOx emissions, refractory wear, and fuel-price exposure. Spec it for throughput-driven secondary smelters where natural gas is cheap and stable, not for s
Gas-fired aluminum melting furnace installation demands refractory-lined chambers rated to 1200°C, PLC+instrument control, and 8-burner high-speed staging on a 7000×5000×3500 mm cell footprint. This guide maps cell layout, gas train, lining stack-up, and commissioning steps. Acceptance gates are tie
Gas-fired aluminum melting furnaces divide into crucible, reverberatory, and stack-melt types, with sub-classes by heat-recovery (recuperative vs regenerative) and firing direction. Selection follows alloy, melt rate, and energy-efficiency targets.
Line frequency induction furnace total cost of ownership is dominated by refractory lining life, electrical losses, and harmonic mitigation—not the headline purchase price. A 10-ton class line frequency coreless furnace typically costs more to install than a medium-frequency unit of equal melt rate
Line frequency induction furnaces run directly on 50/60 Hz mains, making them the lowest-cost option for melting iron and steel scrap above 1 ton, but stirring losses and poor cold-start efficiency limit them against medium-frequency units. They suit high-throughput ferrous foundries and are wrong f
Line-frequency induction furnaces are the 50/60 Hz mains-frequency coreless units used chiefly for melting cast iron, steel scrap and large tonnage iron baths, with typical furnace capacities from 1 t to 30 t per unit. This guide maps the 2026 installation envelope: foundation, water-cooled copper c

A casting ladle is a refractory-lined vessel used to transfer and pour molten metal from furnace to mold, with capacities typically ranging from 1 ton to over 300 tons depending on steelmaking scale. This article maps its engineering advantages, refractory and mechanical failure modes, and selection
Casting ladles fall into three functional classes — transfer, pouring, and treatment — and span 20 kg hand shanks to 300 t steel-mill teeming vessels carrying metal at 1,350–1,650 °C. Selection hinges on capacity, lining, pour mechanism, and lifting method matched to the metal and process step.

Induction furnace TCO over a 10-15 year service life is dominated by electricity (60-80%), refractory relining, and water-cooled coil upkeep, while the initial capital cost typically represents only 15-25% of lifetime spend.

Coreless induction furnace installation hinges on four checks: refractory lining cure, water-cooled copper coil integrity, parallel capacitor bank tuning for the 0.1-0.3 native power factor, and a hardened supply rated for the high-frequency eddy-current drive. For iron and steel melting, a med

Total cost of ownership for a melting furnace is dominated by energy, refractory life, electrodes, and downtime over a 10-20 year service window. Capex is typically 15-30% of lifetime spend; the remaining 70-85% is opex, making the furnace type and duty cycle the decisive economic lever.
Melting furnace selection pivots on five trade-offs: melt rate vs. energy efficiency, melt quality vs. refractory life, fuel source vs. emissions, batch vs. continuous duty, and capex vs. melt-loss control. Choose induction for clean steel and tight alloy control; cupola for low-cost high-volume iro
Industrial melting furnace installation requires matching furnace type to alloy, duty cycle, and power supply before foundation, water-cooling, and electrical commissioning can proceed. Medium-frequency induction units 10-50,000 kW dominate steel, iron, copper and aluminum melts at 50/60 Hz supply.

Melting furnaces are classified by heat source into induction, gas-fired, resistance, ESR, cupola and crucible types, with selection driven by metal, capacity and melt cleanliness. Aluminium regenerative and induction units dominate 2026 export offerings at US$9,000-108,000.
Zinc die casting delivers castings with 1M+ die tool life, low 419°C melt point, and net-shape thin walls, but the alloys cap at ~120°C service and weigh ~2.5× aluminum. Below is a 2026 spec-side pros/cons brief for buyers comparing hot-chamber zinc against aluminum, magnesium, and gravity processes
A correctly installed zinc die casting machine pairs a hot-chamber shot system with a 5-125 ton clamp on a level foundation, dies anchored to T-slot rails, hydraulic power at 60-80 bar, and dry-cycle commissioning before the first zinc alloy pour. REINER specifies 400x600 mm die space, Z410 (GD-ZNAL

Magnesium die casting machine TCO spans machine class, shot weight, auxiliary gas/cooling, dies, energy, and labor; buyers should weigh 10-year spend lines before choosing between cold-chamber, hot-chamber, and vacuum platforms.

Magnesium die casting machines split into hot-chamber and cold-chamber types by melt feed method, with cold-chamber dominant for production tonnages above ~250T due to melt reactivity; typical machine line-ups run 250T to 1600T clamping force and feed alloys such as AZ91D, AM50/60, and Mg-Al-RE grad
Aluminum die casting machine total cost of ownership is dominated by five cost lines — machine capex, die/tooling, energy, consumables, and labor — over a 5-7 year lifecycle, with 25-ton units priced at $10,000-11,000 and 80-90 ton units at $17,000-22,000 on Alibaba listings as of 2026-07.

Aluminum die casting machines deliver 900 kN-class clamping force in the 10,000-22,000 USD price band, suiting high-volume production of thin-wall, complex parts but imposing steep tooling cost and limited alloy reach. The technology favors aluminum and zinc alloys, with cycle times measured in tens

A correct aluminum die casting machine installation sequences foundation checks, rigging, leveling, hydraulic/electrical tie-in, die clamping and cold-chamber commissioning. Clamp tonnage must match part projected area at 30-70 MPa specific pressure, and utilities (cooling water, hydraulic oil ISO V

Gravity die casting machine total cost of ownership is dominated by five cost lines: tooling (often ~30% of die casting tooling cost), energy per heat, die consumables, refractory life, and labour; TCO over a 5-year run is therefore driven less by the press price and more by die life and cycle time

A gravity die casting machine pours molten metal into a permanent metal mould under gravity alone, with no high-pressure injection, suiting brass, zinc and aluminium alloys at moderate volumes.

Gravity die casting machines are classified by alloy (aluminum, brass, zinc), drive type (manual, hydraulic, PLC-automatic) and mold format (stationary, tilting, rotary), with 2026 OEM catalogs emphasizing PLC+touch-screen hydraulic units for non-ferrous runs from under 1 kg to multi-ton batches.

Low pressure die casting machine (LPDC) CAPEX starts around $10,000-22,000 for 25-80 ton units from Chinese OEMs, but total cost of ownership over a 10-15 year service life is typically 3-5x purchase price when energy, die wear, refractories, and downtime are added.
Low pressure die casting (LPDC) fills molten aluminum into a sealed die under 0.02–0.10 MPa gas pressure, delivering denser, lower-porosity parts than gravity casting but at lower throughput and higher tooling cost than high pressure die casting.

Low-pressure die casting (LPDC) machines split into cold-chamber and hot-chamber subclasses, with continuous and tilt-pour variants, distinguished by chamber design, alloy compatibility, and clamping force, not by maximum injection pressure alone.
Squeeze casting applies 50–150 MPa direct pressure during solidification of liquid metal, producing near-net-shape parts with tensile strength gains of 20–30% over gravity casting, but cycle times of 3–8 minutes and die costs 2–4× higher than gravity dies restrict it to mid-to-high volume runs.

Squeeze casting machine installation hinges on foundation, hydraulic and die-set alignment: SCH-3500-class presses run ~130 MPa peak specific pressure at ~0.085 m/s punch velocity, requiring rigid grouted bases, leveled tie-bars, and matched die preheat above 297 °C to avoid shrinkage porosity.
Squeeze casting machines split into direct and indirect types classified by how pressure is applied to the melt, with vertical and horizontal machine frames and dedicated variants for aluminum, brass and MMC production.

Vacuum die casting machine TCO is driven by vacuum pump train sizing, leak-rate discipline and chamber down-time, not sticker price. Five-year spend typically splits across energy, consumables, maintenance and lost yield from porosity.
Vacuum die casting cuts cavity gas to roughly 50-100 mbar, lifting tensile strength and enabling T6 heat treatment, but it shrinks the process window, demands low-iron alloys and adds sealing/lubricant cost on every cycle.
Vacuum die casting (VDC) installs a vacuum system — typically a 50–500 mbar absolute chamber, two-stage rotary-vane or dry claw pump, and a leak-back rate held under 5 mbar/min — onto a standard cold-chamber or hot-chamber die casting machine. A correct VDC installation drops gas porosity by 30–80%

Vacuum die casting machines split into vertical vacuum-assisted, horizontal high-vacuum, and vacuum-squeeze (VSC) variants, with chamber pressure bands of 0.025-0.080 MPa and typical molten-aluminum holding at 660-720°C for porosity-free structural castings.

Cold chamber die casting machine TCO is dominated by energy, hydraulic oil, die wear and downtime, with acquisition price typically 35-50% of 10-year lifecycle cost across 400-1600 ton clamping-force classes.

Cold chamber die casting machines inject molten metal from a separate furnace into the shot cylinder, enabling high-pressure forming of aluminum, magnesium, copper and brass alloys that exceed hot-chamber melt-pot limits.

Installing a cold chamber die casting machine cleanly is a 5–7 day civil-mechanical-utility-commissioning sequence: foundation pit and anchor bolts, oil-hydraulic routing, tie-bar and platen alignment, then molten-metal interlocks and PLC/IO check. Get platen parallelism, platen-to-platen parallelis

Shot sleeves in die casting extend tooling life, stabilise fill velocity, and cut cold-shut rejects, but raise per-shot cost, demand pre-heat discipline, and accelerate wear on the plunger tip.

Shot sleeves in die casting are consumable molten-metal transfer sleeves press-fit into the cold-chamber gooseneck, with 4140/8620 alloy steel and nitrided or H13 tool steel dominating by alloy class. Proper installation gates on concentricity, interference fit, and pre-heat so the sleeve seats befo
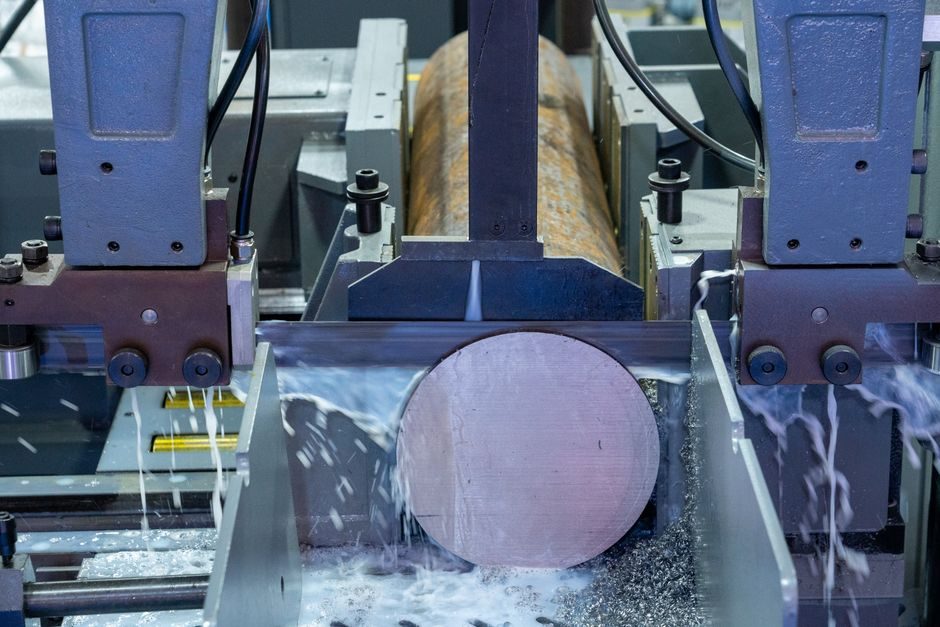
Hot-chamber die casting injects molten low-melting-point alloy through a gooseneck submerged in the bath, with cycle times under one second on small zinc parts; it suits zinc, magnesium, and lead alloys but cannot handle aluminum or copper because iron pickup and thermal attack destroy the pot and p

A hot chamber die casting machine installs in 3-7 working days when the foundation, hydraulic, cooling and zinc-bath utilities are pre-staged; the four installation gates are pit/foundation, hydraulic + cooling tie-in, melt-pot pre-heat, and PLC commissioning.
Hot chamber die casting machines are the dominant choice for zinc, magnesium and lead alloys below ~420 °C, classified by clamping tonnage (400–4,000 t), plunger/shot mechanics and gooseneck immersion design rather than by alloy alone.
Die casting machine TCO over a 10-year horizon is dominated by energy and maintenance, with the acquisition price representing only a single-digit to low-double-digit share of lifetime spend. A working 2026 TCO model covers acquisition, energy, maintenance, consumables, downtime, and end-of-life dis
Die casting machine installation hinges on matching tonnage class to alloy and shot weight, with cold-chamber units (380T–9000T locking force) dominating aluminum structural work and hot-chamber units serving zinc and magnesium under 1 kg per shot.
Die casting machines divide first by chamber design (hot chamber for low-melt Zn/Pb/Zamak; cold chamber for Al/Mg/Brass), then by tonnage, alloy and automation. Sourcing band on Alibaba 2026-07-14: hot-chamber 25-180 ton at $10k-$32k, cold-chamber 80-280 ton at $17k-$50k.
Sanding deburring machines split into abrasive-belt, rotary-brush, wide-belt wet, and planetary/cutter-head families, with working widths spanning 300 mm to 1600 mm and throughput speeds reaching 10 m/min on standard production units listed in 2026 OEM catalogues.
Industrial parts washers split into four main types — aqueous cabinet, high-pressure spray, ultrasonic, and conveyorized pass-through — selected by part geometry, soil type, and production volume. Aqueous systems dominate over solvents for safety and EPA compliance, with custom builds for aerospace,
Global vibratory feeder supply in July 2026 is fragmented across Chinese OEM/ODM hubs, Indian mid-tier makers, and a consolidated European alliance, with bowl feeder export prices ranging US$1,290–12,000 per set and 1-piece MOQ common.
Vibratory feeders split into bowl, linear, step, centrifugal and rotary-table types, with electromagnetic coils typically rated 24–230 V AC / 15–50 Hz driving most modern conveyor and sorting systems; selection is driven by part geometry, throughput, and cleanliness class.
Vibratory feeders are selected by matching drive type (electromagnetic vs motor-driven resonance), trough geometry, and frequency/amplitude to the bulk material's flow behaviour; electromagnetic units suit low-capacity, fine-part feeding while motor-driven resonance units handle 3-300 t/h heavy bulk

Alibaba lists 40,000+ hydraulic-press SKUs from global suppliers, with made-in-china.com indexing 3600t metal-door embossing presses at US$58,000–59,000/set and 315 t trolley presses at US$15,000–20,000/set as of 2026-Q2.

Sheet-metal deburring machines for laser/plasma cut parts span roughly US$5,999–12,000 for entry-level Chinese-built units, US$10,000–30,000 for mid-tier belt/brush edge-rounders, and US$40,000+ for wide-format wet-grinding or robotic cells, with price driven by working width, station count and abra

Forging press selection pivots on drive type (mechanical/hydraulic/servo-hydraulic), tonnage, stroke and die envelope. Servo-hydraulic 3-punch units at 980 kN and 250 bar suit 12-32 mm bar brass/aluminium at 500-3,600 parts/h. Open-die hydraulic presses scale to 50,000-ton class for heavy f
Aluminum coil selection pivots on alloy series, temper designation, thickness range and end-use forming depth; mismatched grades such as 1100-O versus 5052-H32 routinely cause cracking or springback in fabrication.
Pick aluminum sheet by alloy family first: 1xxx/3xxx for formability, 5xxx for marine-weld, 6xxx for structural. Then match temper (O/H14/T6), thickness 0.2–200 mm, and verify ASTM B209 / EN 485 mill cert.
Magnesium die casting part pricing in mid-2026 clusters roughly US$1–20 per piece at 1-piece MOQ and US$1,000–20,000 per mold, with final cost driven by alloy (AZ91D/AM60), part weight, tolerance, and process type (hot-chamber vs cold-chamber).
Zinc (Zamak) hot-chamber die casting is the lowest-cost option for thin-wall, high-volume precision parts under ~3 kg, with typical alloys Zamak 2/3/5/7 (Zamak 3 dominant), 0.05 mm–0.03 mm mould tolerance, and machine tonnage below 160 t for most consumer applications.
Hot chamber die casting machines are specified for zinc, magnesium, copper and lead alloys below ~420°C melt point, with a 30-ton clamping class (Simhope SH-25) typical for small hardware and 3C electronics. Selection gates are alloy compatibility, tonnage, shot weight and cycle time.
Vibratory feeder selection hinges on four gates: drive principle (electromagnetic vs electromechanical vs piezo), amplitude-frequency control, controller current rating, and hazardous-area certification. ATEX-certified electromagnetic units dominate bulk-handling lines; variable-frequency digital co
Industrial oven prices in 2026 span roughly USD 3,000 for small batch batch/convection units to over USD 200,000 for continuous IR tunnel lines, with heat-source, chamber volume and conveyorization driving 80%+ of the spread. Hot-air circulation remains the dominant low-cost architecture, while elec
Industrial oven selection turns on four gates — max temperature, chamber volume class, heat source, and atmosphere class — and the 2026 catalog still anchors on 260–760 °C as the dominant electric bench/cabinet range, with walk-in and conveyor units covering the rest.
Sandblasting service runs $40-$75/hr and $1-$16/sq ft in the U.S. while Chinese-made cabinet machines start around US$800-1,050; full sandblasting rooms list at US$20,000-99,800 per set from Made-in-China.com.

Sandblasting equipment selection hinges on four gates — feed system (siphon vs pressure), cabinet geometry, abrasive media, and dust/ventilation duty. July 2026 supplier catalogs show pressure-blast cabinet pricing from roughly US$320 to US$4,800 and China-made machining-service nozzles at US$1.80–4

Hydraulic press selection hinges on matching tonnage, frame type, stroke length and duty cycle to the workpiece — H-frame for off-center loads, C-frame for side access, 4-post for precision die work.

Forging press pricing spans US$270,000-300,000 for entry-level Chinese cold forging units (MOQ 1 set) up to multi-million-dollar CNC screw presses rated 4,100-102,400 kN like the FICEP DD series; total cost of ownership is driven by tonnage, drive type, and energy recovery architecture.
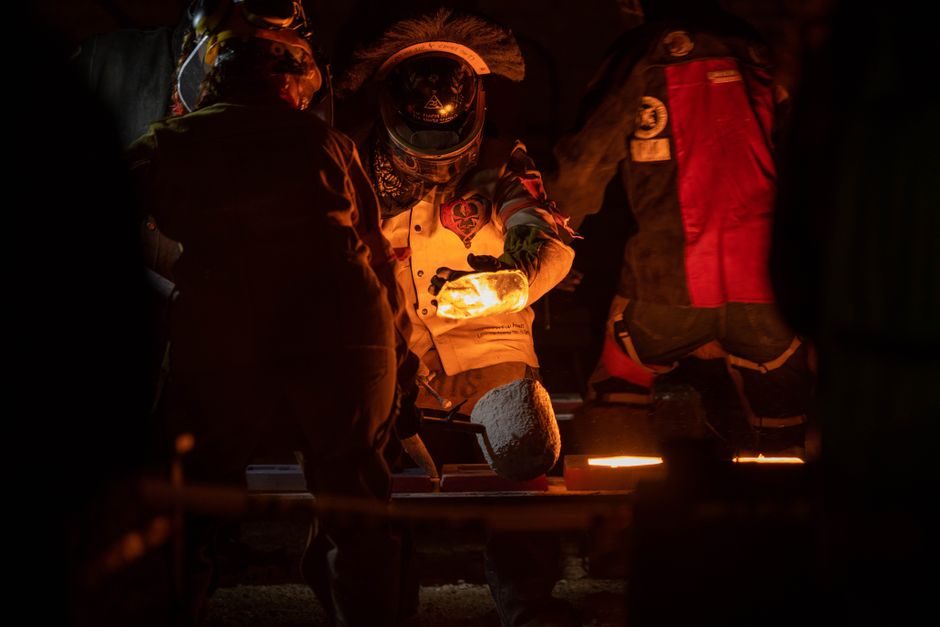
Investment casting equipment capex for a small-to-mid lost-wax line typically spans US$60k–US$300k, dominated by wax injectors, shell lines, dewax autoclaves and induction furnaces. Running cost is driven by colloidal-silica shell chemistry, wax reclaim and energy-intensive burnout/induction melt st

Cast aluminum alloy pricing on Made-in-China in 2026 ranges from US$0.10–US$0.30/kg for raw A356/A380 billet, US$2–US$15/kg finished casting, and US$500–US$9,000 per mould set; alloy family, casting process and Fe content control drive 30–60% cost spread.

Cast aluminum selection is a four-axis decision: alloy family (1xx–7xx.x), casting process (sand, gravity, HPDC, low-pressure), mechanical class, and corrosion environment. A356 and A319 dominate gravity castings; A380 and A383 dominate HPDC; 242.0 is the aviation cylinder-head benchmark.

Aluminum coil spot prices in July 2026 sit in a US$2,200–4,200/t band on Made-in-China listings for stucco/embossed coil, while per-kg anodized coil runs US$6.00–10.00/kg; MOQ 5–15 t, alloy 1050/3003/5052/6061 dominate the China export market.

Aluminum sheet 1050/1060/3003/5052/6061 is quoted at roughly US$1,600-4,000 per ton FOB China as of July 2026, with mill-MOQ 2-5 tons and alloy/temper driving 40-80% of the spread across suppliers like Lingfeng and Chalco.
6063/6061 aluminum extrusion profiles on Made-in-China and ECVV list FOB at US$1,500–3,600/ton; 80/20 T-slot and corner brackets sit at US$1.98–3.30/piece, with 20-ton MOQs and 5,000-ton monthly capacity on bulk window/door extrusion.

6063 T5/T6 dominates architectural and light-industrial extrusion at 6000mm stock length under GB/T 5237-2000, while 6061 T6 and 7075 T6 carry structural and high-strength loads; 2026 spot offers sit near US$2.50-4.00/kg with 300 kg MOQ at audited Chinese mills.

Zinc die casting unit prices cluster around US$0.18–0.36 per piece for commodity hardware, US$1–10 for industrial components, with tool steel tooling often exceeding US$5,000 and Zamak 3/5 driving the alloy decision in 2026.
Aluminum die casting on B2B platforms ranges from US$0.10–$15.60 per piece at 100-piece MOQ, with total project cost driven by alloy, part size, machining, surface treatment and mold amortization.
Aluminum die casting selection hinges on three choices: HPDC vs. LPDC vs. gravity/vacuum process, alloy family (A380, A383, A360, ADC12), and tonnage matched to projected area. Verify ISO 9001, NADCA process monitoring, and post-machining capability before awarding the PO.

Gravity die casting machine selection turns on alloy (Al/Cu/Zn), tonnage class, and PLC/hydraulic control; current 2026 sourcing channels list 25–280T models, $10,000–$50,000 FOB price bands, and ISO 9001/IATF 16949 vendor base in Ningbo.
Cold chamber die casting machine selection hinges on matching locking force (kN), platen size, and shot weight to alloy and projected area; Bühler's Ecoline S spans 3,400–8,400 kN for Al/Mg, while Chinese suppliers like Longhua push 1,600 t class (≈14,700 kN) for large structural castings.

Deburring machine selection hinges on matching the burr type (laser slag, punched edge, sawed flash) to the right process class — abrasive belt, brush roller, wet grinder, or cutter-head chamferer — with working width 950–1650 mm and 0.5–50 mm thickness as the dominant spec envelope seen on 2026 OEM
Industrial aqueous parts washers in the 20-gallon class ship from Chinese OEM listings at roughly 31 kg net with 180 LPH pumps at 220 V/50 Hz, while used aqueous and solvent models commonly resell between USD 500 and USD 5,000 depending on tank size, heater kW and flammables rating.
Industrial parts washer selection in 2026 hinges on matching throughput, contamination type and effluent rules to one of four platforms: aqueous, ultrasonic, vacuum-degreaser, or solvent cabinet — each with distinct ROI and floor-space trade-offs.

Vibratory feeder pricing on China-origin trade platforms spans roughly USD 1,290–1,580 per piece for small electromagnetic units as of 18 June 2026, while life-cycle analyses show vibratory loss-in-weight feeders outlast screw feeders in total cost of ownership for many plastics applications.

A cold box core shooter is the standard amine-gassed, PU-bound sand core machine for aerospace foundries; sizing hinges on 50-100 L shot capacity, 0.4-0.7 MPa air, and core box envelope ≥ 600×500×400 mm for turbine-class work.
Choosing a cold-box core shooter for 2026 foundries: match blowing pressure (typically 0.5-0.7 MPa), amine-gassing cycle, and shot weight to your core box volume, then verify PLC, CE/UL electrical, and sand-mix resin system compatibility before purchase.

Mining-spec shell molding machines run 30-50 kW heating power, 0.5-1.0 MPa shell cure air, 800-1500 mm platen, and resin-coated silica sand 0.18-0.30 mm AFS; shell-core shooters pair with them at 5-25 kg shot weight for wear liners.
Lost foam casting line (LFC) suppliers cluster in Shandong, Zhejiang and Ningbo China, with EPS foam pattern density typically 0.015-0.025 g/cm³ and aluminum LFC holding 0.5-3 kg/cm² vacuum during pour. Verified makers include Qingdao Shengmei, Qingdao Haoyang, Ningbo Tongda, EATHU.
Lost foam casting lines are best specified by annual tonnage, foam pattern size envelope, flask dimensions, and coating station throughput; typical job-shop floors run 1,000-10,000 t/yr at 0.3-0.5 MPa vacuum, with 3,000-30,000 t/yr industrial builds.
Lost-foam casting lines for chemical-processing service centre on EPS pattern quality, vacuum draw, refractory coating control and resin binder selection; Qingdao Shengmei ships one Set/Sets at 1.00 USD/Set FOB with 10 Set/Sets monthly capacity, and a comparison of STMMA, EPMMA and EPS bead systems
Lost foam casting line selection hinges on pattern density, coating permeability, foam grade and metal reactivity; a sand-fill/vacuum molding line with controlled pouring is specified when carbon pickup in low-carbon steel and gas porosity in aluminum alloys are unacceptable.
Static pressure molding machine FOB bands cluster at US$30,000-40,000 per piece for mid-range ZD-series units and US$450,000-1,200,000 per set for full automatic lines, with Qingdao-based OEM factories dominating 2026 export listings on Made-in-China.

A static-pressure molding machine is a foundry line for flaskless sand molds using compressed-air squeeze, and "best for data center" usually means dense, repeatable castings for server-rack castings, busbars or HVAC housings — typically 500–1000 kN squeeze force, 600×500 mm flask size, with PLC/HMI

Automatic molding line FOB price bands run US$58-1,200,000/set in 2026, with static-pressure foundry lines from Qingdao at $450,000-1,200,000 and PE blow-molding sets at $60,000-150,000; sourcing hinges on flask type, PLC control and audited-supplier status.

Automatic molding line sizing hinges on four levers — flask size envelope, shot weight, mold closure force and sand-handling throughput — with throughput bands typically scaling from 30 molds/hr for job shops to 240+ molds/hr on high-pressure DISA-index lines. Spec the line to the part mix first, no

Automatic molding lines for power-generation castings span flask sizes of roughly 800×600 mm to 1600×1200 mm, with cycle rates of 12–30 molds/hour on greensand and 180–400/hour on horizontal flaskless, selecting on part weight, alloy and takt.
An automatic molding line for sand foundries is selected on five hard numbers: flask size, mold height, sand-feed rate (t/h), squeezing/jetting pressure, and cycle time; resin PU, green sand and shell lines split on those axes, with DISA vertical and SINTO horizontal as the two reference platforms t

For automotive foundries, the best sand mixers in mid-2026 deliver 30–60 t/h throughput on resin-bonded or green sand, with shaft power from 18.5 kW (lab) to 75 kW (production), dual-hydraulic drive and bottom-discharge doors. Selection must match binder chemistry to casting size, not chase maximum

Foundry core making machine sourcing in 2026 is dominated by Shandong, Qingdao and Jiangsu manufacturers on Made-in-China.com, with sand core making machines typically priced US$3,000–120,000 per set and cold-box, hot-box, shell-core platforms clustered around 3-5 kW drives.

Core making machines for semiconductor-grade quartz and silicon-ceramic component foundries are dominated by shell-process and hot-box lines, with benchtop outputs of 30-60 molds/hr and resin-bonded cold-box cells scaled to 100+ molds/hr for volume runs.
Core making machine selection hinges on four binding criteria: binder chemistry (clay/resin/cold-box/hot-box), matched shot capacity, cycle time per core, and curing energy source. Get any of those wrong and the rest of the foundry line pays for it in scrap and downtime.

Stainless 304/316 hygienic automatic molding lines, IP65-rated conveyors and shell-molding equipment are specified for food and beverage plants; selection pivots on wash-down tolerance, surface finish and CIP compatibility.

Degassing and refining unit suppliers concentrate in three clusters: Chinese process-vessel fabricators on Made-in-China, Indian specialty-chemical groups, and EU metallurgy-focused engineering shops. Buyer-side selection hinges on ladle capacity, melt mass, slag chemistry, and target hydrogen or su

Foundry degassing units for aluminium melts are sized on melt mass, target hydrogen level and rotor type; rotary degassers with argon-nitrogen blends dominate, cutting hydrogen to ~0.10-0.15 ml/100 g Al when the bubble residence time and rotor speed are tuned to the bath.
Crucible furnace sizing hinges on charge mass, melt temperature, and metal chemistry: a 6-ton medium-frequency electric crucible melts brass, copper, steel, iron, and aluminium scrap at industrial scale, while smaller hydraulic-tilting aluminium units ship at 1-set MOQ with 50 sets/month capaci

China-domiciled holding furnace suppliers cluster in Guangdong, Jiangsu and Shanghai, with listed FOB unit prices spanning US$10,000 (1 t small electric) to US$500,000 (multi-tonne induction holding lines) on 1 Set MOQ terms as of 2026-04-21.

A holding furnace (保持炉 / 保温炉) is sized by tap weight, alloy, holding temperature window, and allowable metal loss — typically 0.1–0.3 %/h burn-off for Al, with refractory-lined electric resistance or coreless induction bodies dominating the 1–20 t die-casting and extrusion bracket.

Coreless and channel-type induction holding furnaces from makers such as Pioneer Furnaces dominate non-ferrous foundries, while pulp-and-paper mills use holding/soak vessels primarily for calender roll shells, black-liquor equipment and cast-iron dryer head frames, not for fibre stock.

Gas-fired aluminum melting furnaces from Chinese OEM/ODM suppliers cluster in Henan, Jiangsu and Hunan at FOB bands from RMB-ex-equivalent single-digit thousands for sub-1 t units to over US$30,000 for 1+ t reverberatory lines, with 1700°C nitrogen-atmosphere and 2006/42/EC compliance now common spe

Aerospace-grade aluminum melt typically demands a tightly specified gas-fired furnace platform: 720–760 °C melt bath, controlled air-fuel ratio with ≤5% excess O2, low-velocity regenerative or oxy-fuel burners, and refractory lined with ≤4% MgO castables. This article compares the realistic options
Specifying a gas-fired aluminum melting furnace hinges on matching furnace type (reverberatory, regenerative, or crucible) to melt rate, alloy range, and energy cost; regenerative burners cut gas consumption in holding mode but raise control complexity and capital cost.

Line frequency induction furnace sourcing in 2026 is dominated by Chinese OEMs offering crucible-type vertical units in the 100–3,000 kg class at US$10,000–100,000/set FOB, with audited ISO 9001:2015 suppliers clustered in Shandong, Jiangsu, Shaanxi and Henan.
Line-frequency (50/60 Hz) induction furnaces suit marine foundries melting 1-10 t of steel, copper or aluminium scrap per heat on ship-repair or offshore yards, with coreless designs dominating and Chinese OEM export pricing on 500 kg medium-frequency steel-shell units sitting in the US$11,600-12,50
Line-frequency (50/60 Hz mains-frequency) induction furnaces are specified for foundries melting iron, steel, copper and aluminium in the 0.25 t to 5 t-plus range, with 1 t iron-melt units in China priced at roughly US$10,000 to US$1,000,000 per set depending on configuration.

Induction furnace sourcing in 2026 clusters in China: Alibaba lists 500 kg-class suppliers, Made-in-China indexes 58 electrical induction furnace makers across 174 SKUs, with MOQ 1-piece IF units priced US$100,000-1,000,000 from Gold-tier audited suppliers like Xi'an Sanrui.
Sizing an induction furnace comes down to matching kW rating, melt rate (kg/h or t/h) and crucible capacity to your metal, duty cycle and grid; medium-frequency (150-2500 Hz) coreless units dominate ferrous foundries, while channel furnaces suit high-tonnage holding.
An induction furnace is selected by matching melt mass, alloy chemistry and grid frequency to the right coil topology, with 2026 China OEM price bands running roughly US$2,000 to US$80,000 per 1-set MOQ depending on power class and metallurgical duty.

Sizing a melting furnace starts with hourly throughput, charge material, and target superheat, then narrows the choice among crucible, induction, cupola, and gas-fired aluminum furnaces rated between 700°C and 1,400°C.

Chemical processing demands corrosion-resistant alloys (Hastelloy, Inconel) and atmosphere-controlled melting; induction and vacuum furnaces dominate the spec sheet at 1100-1700°C.

Zinc die casting machine supply in mid-2026 is dominated by Chinese cold-chamber and hot-chamber OEM clusters in Ningbo, Dongguan, Qingdao and Lijiang, with locking force spanning 20-1,600 ton, shot weight 0.1-30 kg, and audited ISO 9001 factories competing on mould price (US$0.30-15.00/pc) and mach

Sizing a zinc die casting machine comes down to four numbers: locking force (tonnage), shot weight, platen size, and cycle time. Hot-chamber units dominate below ~100 t, cold-chamber enters when aluminum or magnesium joins the mix.

Spec a zinc die casting machine by matching shot weight, locking force, platen size and cycle rate to part geometry; hot-chamber units dominate sub-7 kg zinc work, and full-automatic lines hitting 35 cycles/min are now baseline in Chinese supplier builds.

Magnesium cold-chamber die casting machines are concentrated in 5 Chinese OEM clusters, with clamping forces spanning 400T-1250T and new-build fully automated units landing near US$258,850 ex-works as of mid-2026.
China dominates the 2026 aluminum die casting machine supply map, with cold-chamber tonnages from 1250 t to multi-thousand-tonne platforms priced US$258,850-258,950 (MOQ 1 piece) and ancillary aluminum die-casting work as low as US$1.00-1.50/piece from audited Diamond Members on Made-in-China.

Aluminum die casting machine sizing hinges on four gates: locking force (kN), platen size, shot weight, and injection pressure profile. Match each to part projected area, alloy, and required cycle time before comparing suppliers.
China hosts the bulk of gravity die casting machine supply, with verified cluster hubs in Ningbo, Quanzhou and Anhui offering automatic lines from US$8,000 to US$400,000 and supporting aluminum, zinc and brass gravity casting with CNC finishing.

Gravity die casting machines for brass, zinc and aluminium are typically specified at 6,000–35,000 USD/set, 1 Set MOQ, with PLC+touchscreen control and per-mold cooling timer; sizing is driven by shot weight, platen area and alloy rather than clamp tonnage.

For semiconductor tooling and heat-spreader prototypes, a vertical-parting gravity die casting cell with 80–250 kN clamp force, hardened H13 tool steel dies, and PLC-controlled tilt-pour delivers the cleanest, lowest-porosity castings when shot weight stays under 5 kg and cycle time can sit above 30

Low Pressure Die Casting Machine sourcing in 2026 is dominated by Chinese OEMs at 1-100 pc MOQ with US$ 0.90-15.60 per-part pricing, plus European tier-1 names like Bühler, Kurtz and OTTO JUNKER holding the high-tonnage bracket above 9 machines per active catalog line.

Low pressure die casting machine sizing hinges on shot weight, platen/clamp force, furnace capacity and cycle time. Selection aligns part envelope, alloy and annual volume with machine class and safety code GB 24391-2009.

Food-grade low pressure die casting machines are typically gravity- or low-pressure aluminium rigs with stainless contact parts, NSF/3-A-style hygienic finishes and 20-200 kN clamping; pricing spans USD 8,000-35,000 for compact units and six figures for full lines.
Squeeze casting machine supply in 2026 clusters in Ningbo, Anhui and Guangdong, with ISO 9001 / IATF 16949 factories offering vertical and horizontal units from roughly 1600 kN to 8000 kN clamp force for aluminium, brass and automotive HVSC parts.
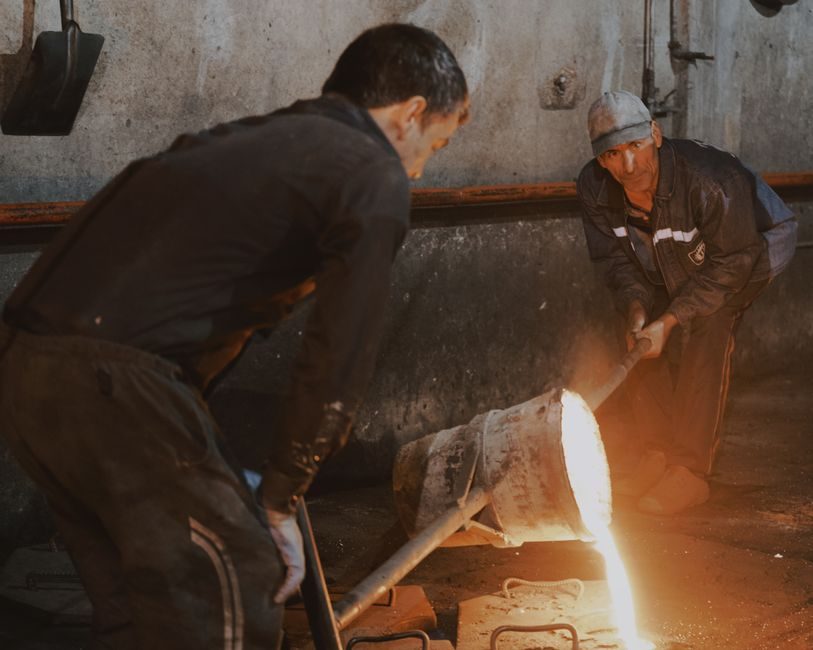
Squeeze casting machine sizing hinges on three coupled gates — clamp/pressing force, shot sleeve diameter vs shot weight, and specific pressure on the casting — with published studies using 25-ton hydraulic presses and 60–90 MPa squeeze pressures on Al alloys. Selection is alloy- and defect-driven:

Squeeze casting machines are metallurgical forming presses, not pharmaceutical packaging equipment; the correct pharmaceutical match is a blister packing machine, with Jornen, Hualian and Veena among active 2026 suppliers.

Squeeze casting machines combine high-pressure injection with sustained static dwell pressure (typically 50-150 MPa) during solidification, eliminating shrinkage porosity in aluminum, magnesium, and brass components. Selection pivots on clamp force, shot weight, intensification pressure, and die env
Vacuum die casting machine sourcing in July 2026 clusters around Anhui, Guangdong, Jiangsu and Shandong OEMs, with horizontal cold-chamber tonnages from 200T to 1250T and vertical vacuum units priced in the US$80,000–800,000 band per.
Vacuum die casting machine sizing hinges on four numbers — clamping force (kN), shot weight (g), vacuum level (mbar) and die envelope (mm). Mismatches between vacuum pump capacity and chamber volume cause porosity above 0.5 mbar residual pressure, the dominant defect in thin-wall aluminum and zinc s

Vacuum die casting machines supply cast pump housings, valve bodies, filter brackets and aerator rotors for water treatment skids; selection turns on clamping force tier, vacuum level ≤50 mbar, alloy (Al/Si, Zn, Mg) and shot weight envelope.

Vacuum die casting machines pull 100-500 mbar absolute pressure inside the die before injection, eliminating gas porosity in aluminum and magnesium structural parts; cold-chamber and magnesium-rated builds with vacuum below 50 mbar are the dominant spec for chassis and aerospace buyers.
Cold chamber die casting machine supply in 2026 is dominated by Chinese OEMs in the 800-12,500 kN clamping-force band, with Taizhou, Dongguan and Ningbo clusters leading the export catalogue and standard builds shipping with Mitsubishi-class PLCs and ISO 14000 environmental systems.

Cold chamber die casting machines (200-9000 kN clamping force) suit oil and gas aluminum/zinc alloy valve bodies and fittings. Selection pivots on platen size, shot weight, intensifier pressure and NACE MR0175 material compatibility.
Cold chamber die casting machines handle aluminum, magnesium and copper alloys above 400°C with shot forces from 200 to over 900 tonnes, sized to projected part area, alloy, shot weight and required injection pressure.

Shot sleeve sourcing sits at the intersection of die-casting consumables and engineered refractories: 1,000–50,000-piece monthly OEM runs from China dominate the global supply, with H13 tool-steel, ductile iron and nitrided grades forming the spec tiers buyers compare on.
Hot-chamber die-casting machines are dominated by Chinese OEM and supplier ecosystems, with 1,246 active Alibaba listings, 50 sets/month CNBM supply capability, and SH-25 class zinc units from CENS-exporting suppliers; key spec anchors are clamping tonnage, shot weight, and alloy family (Zn/Pb/Sn).

13 industrial die casting machine manufacturers are currently indexed on DirectIndustry with 52 product listings; Bühler, Shibaura Machine, Yizumi, Kurtz and Lanson lead the supplier count, while Chinese OEM listings on Made-in-China.com span 160-ton aluminium cold-chamber units at USD 41,220-50,980
Die casting machine sizing and selection hinges on locking four numbers — locking force (kN/tonnage), shot weight, platen size and die stroke — to the part's projected area, alloy, and shot volume; hot-chamber suits zinc/magnesium below ~1600 kN, cold-chamber covers aluminum and brass from 900 kN up
Squeeze casting machines are specified by direct-acting vertical hydraulic presses rated 50-800 ton clamping force with 50-150 MPa intensification pressure on the melt, selected when porosity targets fall below 1% and tensile elongation must exceed 8% in Al-Si alloys such as A390 and A356.
Shot sleeves for cold-chamber die casting are specified by bore, length, material and thermal protocol, with 2026 wholesale unit pricing ranging roughly $80–$400 across standard H13 and ductile-iron grades.
Sand reclamation units regenerate 60–90% of used foundry sand via thermal or mechanical processing, while fettling grinders remove 2–8% of casting mass as grinding dust; the two are sequential, not substitutable steps in a green-sand or no-bake foundry line.
Shell molding machines and static pressure molding machines answer different production problems: shell molding targets thin-walled, high-surface-finish cores and small-to-medium batch runs at 0.2-0.6 MPa squeeze pressure, while static pressure molding is built for high-throughput flaskless green-sa
Gravity die casting machines are PLC + touchscreen-controlled hydraulic cells rated 50-2000 kN, used for brass, zinc and aluminum alloy mould-fill under gravity; selection hinges on alloy, shot weight, mould size, cycle time and OEM support.
Mold base price bands in mid-2026 span roughly $1,200 for a small LKM-type standard frame to $18,000+ for a large HASCO or DME 718/2738 pre-hardened assembly, with steel grade, cavity count, tolerance class and lead time driving 60-70% of the variance.
China-origin mold base suppliers in 2026 quote S50C LKM-type standard sets in the 30%-40% gross-margin band; non-LKM built-to-print frames need 4-5% die-steel upcharge and 30-day tooling lead.
A die-casting die is a hardened steel tool that defines casting geometry, gating, cooling and ejection — typically H13 tool steel at 48–52 HRC, with service life of ~100k shots for aluminum and ~1M+ for zinc, costing USD 5,000–80,000+ in 2026.
Die-casting die selection pivots on part alloy, annual volume, dimensional tolerance and surface finish targets. Cold-chamber tooling for aluminum/magnesium, hot-chamber for zinc; tooling steel grade, shot count life, and cooling line layout are the dominant 2026 buy-side decisions.
Riser cutting machine pricing spans roughly US$3,500–60,000 in 2026 channels, with hydraulic pedestal units clustering at the low end and CNC/robotic cells above US$25,000; total cost-of-ownership hinges on blade type, table load and downstream conveyorisation.
Foundry riser cutting and sand reclamation are different process islands: riser cutting removes the feeding head from a cooled casting using abrasive wheels or hydraulic shear, while a sand reclamation unit regenerates used foundry sand via crushing, magnetic separation, thermal or mechanical attrit
Sand blasting machines span US$75 for a 24-gallon portable unit to US$50,000 for a continuous-pass roller-conveyor steel-plate blaster, with most conveyor/rotary-table industrial systems clustering between US$6,980 and US$15,000 FOB China.
Sand coolers and heat treatment furnaces solve opposite thermal problems: the cooler drops returning foundry sand from 200-300°C to under 50°C in minutes, while a heat treatment furnace ramps a metallurgical load through 800-1200°C on programmed profiles. Spec the wrong one and throughput or hardnes
Shakeout machine selection hinges on four cast-process variables — flask/casting weight, sand type, mold geometry and downstream cooling — that set the vibration class, deck load and drive technology. Match a vibratory or impact shakeout to those variables before comparing price.
Sand reclamation units for foundry return sand swing between 20-150 t/h throughput, three process families (pneumatic, mechanical-attrition, thermal), and 30-80 percent AFS clay/binder removal efficiency. Specifying engineers should match feed moisture, contamination level, and downstream sand coole
Shell core shooters use compressed-air expansion to propel resin-bonded sand into a heated core box, producing thin-walled shell cores in 5-30 second cycles for iron, steel and non-ferrous foundries. Selection hinges on core weight, shot pressure, heating power and tooling standard.
New shell molding machine prices in 2026 span roughly US$8,000 for benchtop semi-automatic units to over US$120,000 for fully automatic four-station production lines, with the median 3-5 t/h foundry-class machine landing in the US$28,000-55,000 FOB-China band.
Foundry sand mixers in 2026 split into two camps — continuous high-speed muller/auger units for greensand and batched resin-bonded mixers with screw dispensers — selected on batch size, binder chemistry, and discharge consistency.
Zinc hot-chamber HPDC and low-pressure die casting (LPDC) target different alloy/melt pools — Zn ≤ 450 °C hot-chamber is the throughput path for Zamak parts under ~10 kg, while LPDC is the structural-Al path at 650-700 °C. Pick by alloy, shot weight, porosity tolerance, and tonnage class.
Magnesium die casting machines in 2026 split into hot-chamber (Mg) and cold-chamber (Al/Mg) platforms, with hot-chamber favored for thin-wall Mg parts under ~5 kg and cold-chamber chosen for larger structural castings; selection pivots on clamping force, shot weight, and shot speed.
Standard aluminum cold-chamber die casting machines operate at 800-9000 kN clamping force with atmospheric venting, while vacuum die casting variants add sealed dies and evacuation to 50-100 mbar absolute, eliminating porosity in structural parts; pick vacuum when tensile and pressure-tight properti
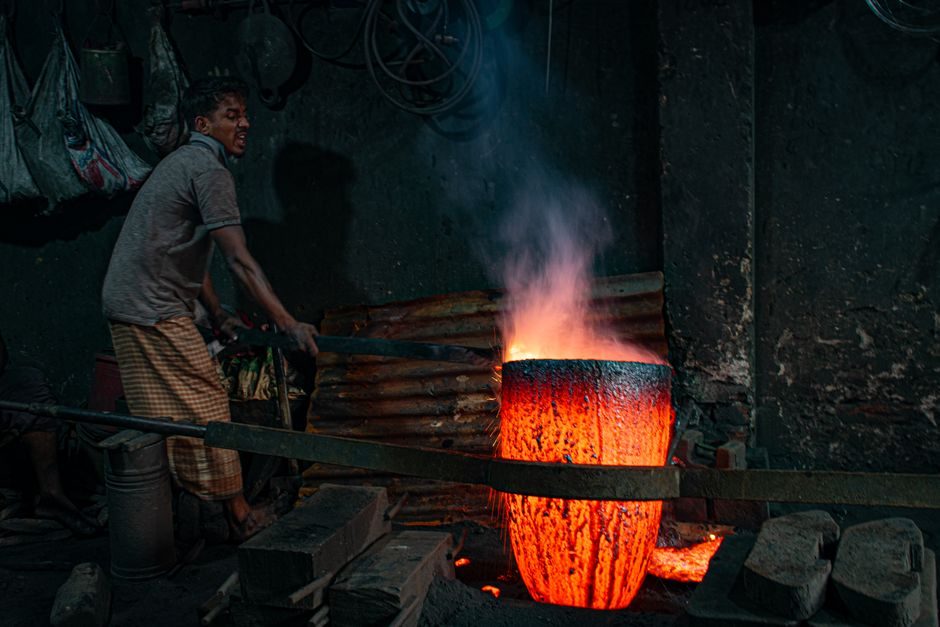
Gravity die casting and cold chamber die casting occupy two distinct slots on a process engineer's selection matrix: gravity (permanent-mould, low-pressure fill) suits brass and zinc at modest tonnage, while cold chamber (high-pressure fill, 300-900T) handles aluminum and magnesium. Match the alloy,
Low-pressure die casting machine selection is driven by six specs: clamping/holding force class, platen size, alloy envelope (Al/Mg), furnace and crucible sealing class per GB 24391-2009, control architecture (PLC + dual-proportional hydraulics), and shot/cycle throughput.
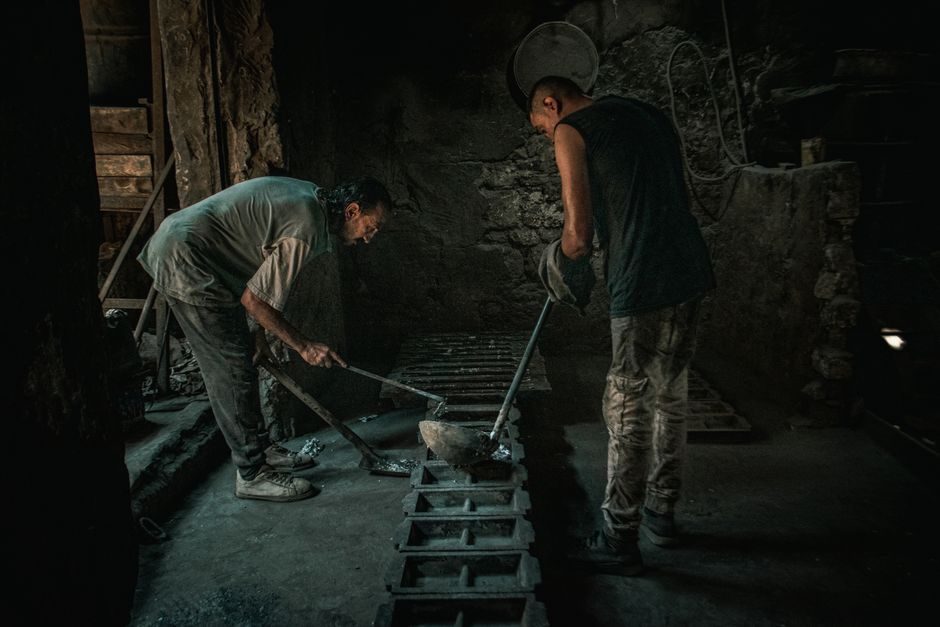
Squeeze casting combines high-pressure die casting tonnage (typically 50-300+ tonnes clamping force) with low-pressure slow-fill (often under 0.5 m/s) to yield near-zero-porosity aluminum and brass components per ASTM B969-2009, suiting structural wheel hubs and valve bodies where high-pressure die
Vacuum die casting machines evacuate die-cavity air to below roughly 50-100 mbar before injection, cutting gas porosity in Al/Mg castings versus standard die casting machines that fill with entrapped atmospheric air at 50-300 mbar cavity pressure.
Vacuum die casting machines evacuate die-cavity air to roughly 50–100 mbar absolute before injection, cutting porosity in Al/Mg structural castings; in 2026 Chinese OEM vacuum units span US$80,000–800,000, with locking forces typically 180–9000 kN for structural parts.
Cold chamber die casting machines for aluminum/magnesium run $40k–$300k+ depending on clamping tonnage (160T–1600T) and automation. Real 2026 sourcing shows made-in-china 160-ton aluminum units at $41,220–$50,980 set FOB, with 500T+ jumping above $113k, plus tooling/peripherals on top.
A 2026 die-casting shot sleeve in H13 tool steel (50–80 mm bore) lands between USD 280–900 FOB China in low volumes, dropping to USD 120–400 at 100-piece runs. Price is driven by bore, steel grade, nitriding depth, and whether a plunger tip is integrated.
A 2026 hot chamber die casting machine in the 25-ton class lists around US$1,000-1,200 per ton on Alibaba, while full OEM/ODM cold-chamber builds range US$41,220-50,980 per set, and landed cost is driven by tonnage, alloy and supply path.
Hot-chamber die casting machines in 2026 are specified 16-180 tons clamping force, served by 1,246+ Chinese suppliers, with new units commonly banded US$25,800-64,500 and used/refurbished lines available below that range.
Hot chamber die casting machines are built for low-melting-point zinc, lead and Zamak alloys, with KYLT's product line spanning 12T to 30T clamping force. Selection pivots on alloy class, shot weight, clamping tonnage, platen size, injection speed, plumbed hot-oil temperature control, and duty cycle
A mold base is a standardized steel frame (A/B/C plates, support pillars, guide bushings) sold as a stock assembly; a die casting die is a one-off engineered tool with shaped cavities, cooled inserts, ejector systems and slide action built around that frame for aluminum, zinc or magnesium HPDC.
Sand casting mold pricing on Chinese B2B platforms in mid-2026 spans roughly US$0.80–10.50 per piece depending on alloy, tolerance and MOQ, with resin-sand machine-tool castings at US$3.00–6.00 and tight-tolerance brass parts at US$7.58–8.89.
A sand casting mold is the expendable, geometry-defining tooling produced per part, while a mold base is the reusable, standardized steel frame (A/B/C plates, guide pillars, bushings) that carries injection or die-casting tooling. Engineers confuse the two on BOMs and lead times; the two follow comp
Green-sand, resin-bonded (no-bake), shell and lost-foam sand casting molds cover different weight, tolerance and lead-time bands from US$1/kg (MOQ) blanks to US$10/piece CNC-finished stainless castings, with simulation and embedded sensor QA now standard at engineering-grade foundries.
Die casting die (tooling) prices span roughly $500 to $15,000 for simple moulds on Made-in-China listings, with the final cost driven by cavity count, slide action, steel grade, and required shot count.
Shell core shooter prices span ₹50,000 to over ₹3,000,000 in 2026, driven by shoot weight, platen size, heat class, and pneumatic-versus-hydraulic actuation. Indian SMEs anchor the entry tier, while European and Japanese lines hold the high end.
Wholesale casting moulds on Made-in-China (June 2026) span roughly US$500-4,000 per piece MOQ, with custom die casting moulds for aluminium alloy at US$500-2,000 and roto-mould flower-pot tools at US$3,500-4,000; a 2026 buying decision hinges on process, material grade, cavity count and steel source
Heat treatment furnaces in 2026 span gas, vacuum and electric models from US$1,200 to US$800,000, with chamber volumes from 10 L to 260 L and max temperatures from 600 °C to 1,100 °C. Spec-driven sourcing beats price-driven buying every time.
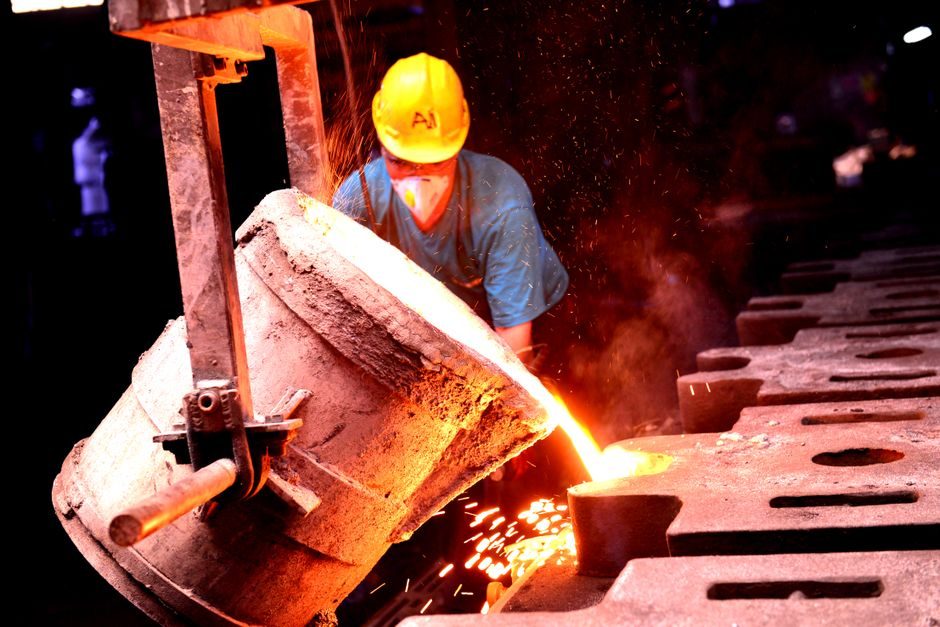
Aluminum die casting machine buying in 2026 hinges on clamping tonnage, shot weight and alloy match; entry-level 25-ton hot-chamber units list at US$10,000-11,000, 80-ton aluminum cold-chamber presses sit at US$17,000-22,000.
A 2026 small-to-mid cupola furnace (1–10 t/h melt rate) for grey iron or brass typically lands between US $35,000 for a used water-cooled hobby unit and roughly US $450,000–$700,000 for a new water-cooled, refractory-lined production stack from a Chinese or Indian OEM, with a hot-blast or recuperate
Lost foam casting and automatic molding lines diverge on pattern logic, parting line and labor intensity; LFC delivers near-net geometry for low-to-medium volume complex steel and iron parts, while flaskless automatic molding lines sustain high-volume green sand production with cycle times under 60
Resin sand molding line buying in 2026 is driven by flask size, throughput tonnage and reclamation loop design; Chinese suppliers cluster on Made-in-China and Alibaba, with matched molding line and sand mixer quotes around US$3-6 per kg finished casting.
A degassing & refining unit (also termed a ladle-degassing or in-line fluxing station) is a metallurgical vessel or station that removes dissolved hydrogen and entrained oxides from molten aluminium or steel. Selection in 2026 hinges on melt mass, target H level, refractory class and process mode.
Shell core shooters and cold box core shooters both use compressed air to fill a core box, but shell equipment cures phenolic resin with 200-300 C heated patterns while cold box equipment cures phenolic/PU resin at ambient temperature with amine gas (ISO 15712 / V Process). Selection hinges on core
New die casting machines from Chinese tier-1 makers cluster in three price bands — US$ 41,000–65,000 for 160-ton cold-chamber aluminium units, US$ 113,000–156,000 for 280–800-ton systems, and US$ 258,000+ for 1,250-ton radiator-class machines — with the spend gap driven by clamping force, shot weigh
Induction furnaces (medium-frequency coreless, channel-type) and cupola furnaces serve different melt-shop roles: induction suits <100 kg to ~100 t clean-steel, iron and non-ferrous melts with tight composition control; cupola remains a 1–80 t/h coke-fired iron-melting workhorse where cheap charge a
A degassing & refining unit removes hydrogen and inclusions from molten aluminium through active injection of argon/nitrogen and flux chemistry, while a holding furnace is a passive thermal buffer that keeps melt at pouring temperature between the melting and casting stations. Spec the unit when hyd
Selecting a shell core machine for a water-treatment plant hinges on shot weight, platen size, cure time and corrosion-resistant framing, since the resin-bound sand cores feed valve and pump castings rather than water contact parts directly.
Casting mold unit pricing in 2026 spans roughly US$0.10 per piece for low-end Chinese silicone vacuum-cast prototypes up to tens of thousands of US dollars for engineered high-pressure die casting tooling, with material, life-cycle rating, and lead time the dominant cost drivers.
Cold box core shooters and resin sand molding lines target different jobs: cold box for high-dimension cores in medium-to-high volume cores, resin sand line for flask-based molds. AISI H13 tooling erosion, amine vs CO2 curing, and cycle-time ratios drive the selection gates discussed below.
Cold box core shooters in 2026 run on two binder systems (CO2-cured phenolic/amine and amine-cured phenolic/gas), three frame layouts (single-station, twin-station, roll-over), with 5-15 kg core capacity and 0.5-0.7 MPa shooting pressure as the working envelope. Specification, not brochure, drives t
Heat treatment furnaces and shakeout machines serve opposite ends of a foundry process: one alters metal microstructure at 700-1200°C, the other separates castings from sand at ambient temperature. Spec choice depends on alloy family, batch volume, and whether the line is job-shop or continuous.
Selecting a shot blasting machine in 2026 hinges on matching wheel-blaster type to workpiece geometry, batch vs continuous flow, abrasive media and required surface cleanliness, with FOB prices for Chinese-built continuous units ranging roughly US $10,000-40,000.
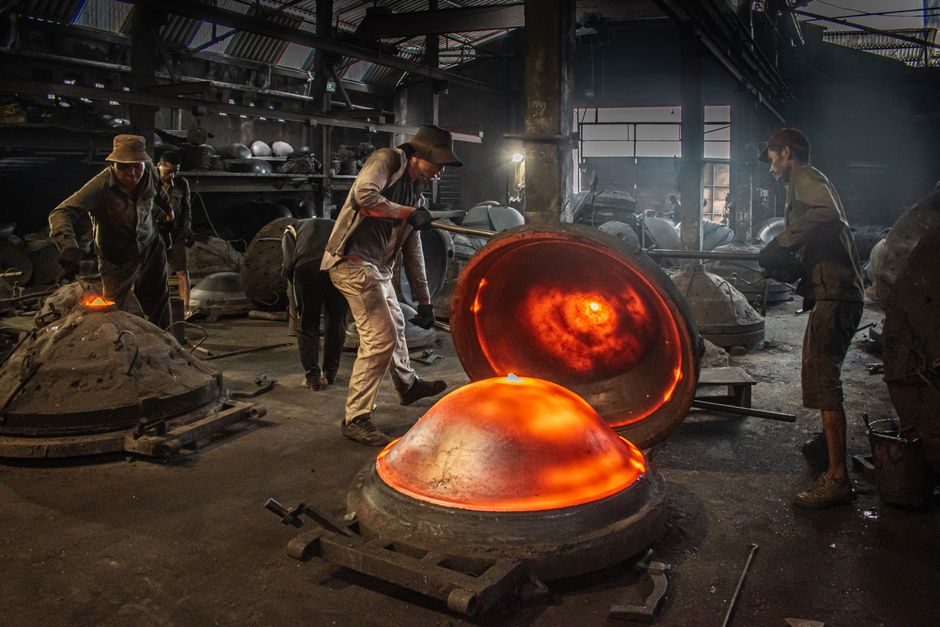
A holding furnace is a thermally insulated vessel that keeps molten metal at pouring temperature between melting and casting; the right class is locked by alloy family, capacity, temperature band, energy source, and refractory duty.
An automatic molding line for foundry use in 2026 lands between roughly US$10,000 and US$300,000 per station for resin-sand and green-sand systems, with the real decision driven by flask size, tonnage, drive type and automation tier rather than sticker price.
Entry-level cold box core shooters in 2026 are quoted in a US $17,000–$18,500 band on Made-in-China for a horizontal/vertical DL-600-B configuration, with hot-box and small-format units dropping to roughly $1,000–$3,000; mid-tier fully automated cold box cells with sand-handling packages run $50,000
Line frequency induction furnaces (50/60 Hz mains-frequency coreless and channel types) remain the lowest-capex route to iron and large-tonnage steel melting, with 2026 China-sourced 1-ton medium-frequency units at US$ 6,550–80,000 per set and 10-ton medium-frequency references near US$ 10,000–100,0
Selecting a melting furnace in 2026 hinges on metal chemistry, melt mass, energy source and refractory duty cycle; induction, crucible, gas-fired aluminum, cupola and holding variants serve distinct production windows and the wrong match inflates kWh/ton and refractory cost.
Squeeze casting machines span roughly USD 25,000 for 300-ton direct-pressure presses to USD 350,000+ for 1600-ton vertical hydraulic rigs, with cost driven by clamp tonnage, platen size, control architecture and alloy-specific tooling. Specifying against ASTM B969 for aluminum-alloy castings locks t
Shot blasting machines in 2026 span hook, roller-conveyor, rotary-table, wire-mesh-belt, catenary and H-beam wheel-blast configurations priced US$20,000–2,000,000 FOB, with 46 manufacturers listing 365 models on DirectIndustry. Selection turns on part geometry, abrasive, throughput, blast-pot c
Hot box core shooters cure resin-bonded sand cores at 200-260°C inside heated tooling, while V-process vacuum molding lines bond dry unbonded sand under a -0.06 to -0.08 MPa film at room temperature. The two systems answer different job-shop realities — one is a high-rate warm-box core cell, the oth
As of 2026-06-26, complete molding line packages on Chinese export platforms span roughly US$4,500 for a single plastic-injection mold and US$90–1,380 per set for smaller molding machines, with full turnkey automatic lines commonly reaching US$50,000–500,000+ depending on tonnage, automation and aux
Line frequency induction furnaces run at mains 50/60 Hz, suit iron and aluminium scrap with capacities from 0.1 t to 10 t, and trade stirring for cheaper rectifier-free builds versus medium-frequency melting furnaces that operate at 1–20 kHz.
Static pressure molding machines for foundry work span roughly $28,000 to $220,000 new depending on flask size, platen force and automation; the 2026 buy hinges on flask dimensions, clamping force in kN, and green-sand or resin-bonded process fit rather than headline price.
Sand blasting machine selection in 2026 hinges on matching delivery (suction vs pressure vs wet vs dry), cabinet class, abrasive media, and dust collection to the workpiece. Entry portable units sit near US$75-85 per piece on bulk channels, while automated drum and tumble systems run US$25,000-
Zinc die casting machines list in a 2026 spread of roughly US$8,000–35,000 for small/medium hot-chamber units, while China-sourced zinc-alloy cast parts sit at US$0.30–15.00/kg-piece tier; total cost is driven by clamping tonnage, shot weight, hot- vs cold-chamber architecture and alloy mix.
Industrial melting furnace prices in mid-2026 span US$5,999-258,000 FOB China depending on type, capacity and alloy, with small electric/professional units at US$5,999-20,500, medium induction sets at US$7,500-12,500, and large aluminium melting/homogenizing lines at US$103,000-258,000.
An automatic molding line is best scoped as a 5-axis spec, not a price tag: line type, hourly output, station count, control package and auxiliaries drive a 2026 China-floor spread from roughly US$ 19,500 (chocolate bar, single-piece MOQ) to US$ 92,000,000 (large plastic-pipe extrusion line, 1 set M
Industrial holding furnaces in 2026 span US$1,000–US$300,000/set across box-style, induction, gas-fired and crucible types; selection hinges on melt type, capacity, refractory class, and energy source, not headline price.
Hot chamber die casting machines run zinc, lead, and magnesium alloys with submerged goosenecks, while aluminum die casting machines are cold-chamber designs that inject molten aluminum into a separate shot sleeve; pick by alloy chemistry, not by throughput alone.
Industrial foundry sand mixers from Chinese suppliers list FOB prices between roughly US $3,000 and US $40,000 per unit, with the model, batch capacity and drive configuration driving the spread. Buyers should match selection to sand system throughput and resin or binder chemistry rather than chase
Die casting dies and sand casting molds are two fundamentally different tooling systems: a die is a reusable steel tool for high-pressure injection of non-ferrous alloys (Al, Zn, Mg) at 10-100+ MPa cycle, while a sand mold is a single-use bonded silica mold for lower-pressure pouring of nearly any a
Vertical automatic shell core machines in the 8-25 kg single-shot class cover 70-90% of foundry duty, with platen sizes from 550x400 mm to 1100x900 mm, cycle times of 25-45 s and 0.4-0.7 MPa shooting pressure governing the 2026 selection cut.
Turnkey lost foam casting lines from Chinese suppliers list from roughly USD 100,000 to over USD 1,000,000 depending on flask size, foam density control and vacuum degree, with EPS pattern tooling, coating booth and sand reclamation as the dominant cost levers.
Industrial sand cooler prices in 2026 span roughly USD 8,000 to 120,000 per unit, driven by throughput (5-80 t/h), cooling media, refractory lining and dust-control integration. This guide breaks down the cost levers a foundry or resin-sand line buyer must weigh before issuing a PO.
Holding furnaces hold and temperature-condition bulk melt in a stationary vessel; casting ladles transfer a metered, refractory-lined pour stream between furnace and mold. Pick by melt mass, temperature delta tolerance, and metallurgical duty.
Low pressure die casting (LPDC) machines push molten metal at 15-100 kPa into steel dies per GB 24391-2009. 2026 selection hinges on clamping force, platen size, alloy family, and safety compliance.
A 2026 shell core machine buy balances shot weight, cure method, and tooling footprint; vertical automatic units dominate batch output while benchtop gear suits short-run job shops, with vendor sources active as of 2026-06-22.
Cold box core shooter selection is governed by six spec gates: core weight, amine binder system, parting-line count, cycle time, sand-blow pressure and gassing port layout. Matching these against the casting program determines single-station, three-station rotary or four-way parted architecture.
Low pressure die casting (LPDC) machines and shot sleeves belong to different specification layers: LPDC is a whole casting process governed by GB 24391-2009 safety requirements, while a shot sleeve is a consumable component inside high-pressure cold-chamber die casting. They are not interchangeable
A cupola furnace is a vertical, cylindrical, refractory-lined shaft melter charged alternately with metal, coke and limestone; for 2026 it remains the lowest-cost high-tonnage route for gray and ductile iron, with 1–25 t/h class units still dominant in jobbing and captive foundries.
Listed induction melting furnace prices on Made-in-China.com (2026-04 to 2026-05 listings) span roughly US$1,280 for sub-100 kg mini units to US$129,999 for multi-ton steel/iron melting sets, with 150 kg aluminium-scrap units clustering at US$10,000-15,000 and 1-30 t electric-arc alternatives at US$
A shell core machine is a sand-core shooting unit that blows resin-coated sand into a heated metal box (core box) to cure a shell-like foundry core; selection should start with shot weight, core-box platen size, cure-station heating medium and tooling-clamp force.
Resin sand molding lines and lost foam casting lines solve different casting problems in 2026: resin/furan lines deliver 5-50 t/h high-density sand molds for steel/iron mass production, while lost foam (LFC) lines produce near-net-shape EPS-pattern castings that eliminate draft and parting lines for
Gas-fired aluminum melting furnace selection turns on four hard gates: melt rate (t/h) matched to a refractory-lined crucible or reverberatory chamber, burner type (regenerative, recuperative, or stack), flue-gas heat-recovery device, and melt-loss ceiling. Apply these against charge mix, fuel gas c
Gas-fired aluminum melting furnaces for 500–5000 kg capacity generally list in a US$10,000–80,000 band on Chinese B2B platforms in 2026, with regenerative and tilting reverberatory units pushing past US$100,000. Real delivered cost depends on refractory grade, burner technology, gas pressure, and au
Degassing & refining unit price in 2026 spans roughly USD 8,000 for a 200 kg aluminium-batch rotary unit to USD 80,000+ for a 3,000 kg in-line melt-treatment station, with rotary degassers, in-line SNIF/MINT stations and lance-type units costing out at different throughput and refractory gates.
Specifying a die casting machine in 2026 reduces to six hard gates: alloy family, tonnage class, chamber type, cycle-time budget, shot-slug/shot-weight envelope, and the auxiliaries envelope (spray, robot, vacuum, die-temperature). Match those before quoting; brand choice follows.
Shell core machine selection resolves to seven engineering gates — shot weight, cure temperature, sand type, box size, cycle time, exhaust, and automation — applied before any vendor quote is requested.
Sand mixers prepare resin- or clay-bonded foundry sand, while a molding line is the integrated system that forms, compacts, and closes molds for casting. Selecting between a standalone mixer and a full automatic molding line depends on batch size, sand chemistry, and required cycle time.
Line frequency induction furnaces (LFF) typically cost $8,000-$15,000 per metric ton of melt capacity in 2026, with a 10-ton steel scrap melting unit landing at roughly $80,000-$150,000 turnkey depending on coil tier, refractory lining, and power-factor correction scope.
Foundry degassing units target hydrogen removal and inclusion flotation in aluminum melts, while casting ladles handle transfer, pouring and vacuum refining of steel with refractory-lined cavities. Selection pivots on alloy, hydrogen threshold and temperature regime.
Core making machine selection hinges on four gates: process type (shell, hot-box, cold-box, CO2, no-bake), core weight and box size, hourly throughput target, and resin/binder compatibility matched to a defensible capex band. Match the gate to your casting mix first, then the spec.
Casting molds and sand blasting machines sit on opposite ends of a foundry loop: one shapes molten metal into geometry, the other strips scale and sand off that geometry. This 2026 spec cut lines the two against throughput, abrasive media, dimensional tolerance and process fit, so buyers can match e
Gravity die casting machine pricing in 2026 spans roughly $10,000 for compact semi-automatic units through $120,000+ for large-tonnage automated cells, driven by clamping force, alloy served, and automation tier.
Crucible furnace buying in 2026 hinges on matching melt capacity, maximum temperature, crucible material and heating medium to the metal being poured; budget 800-6,000 USD for entry electric units, 4,000-50,000 USD for mid-size induction, and confirm CE/UL/CCC paths before shipment.
Gas-fired reverberatory furnaces and induction furnaces split the aluminum melting market by tonnage band and melt cleanliness. Reverberatory units dominate large foundries, while induction furnaces now hold the niche for smaller, cleaner batches.
Fettling grinder FOB bands run roughly US$180-1,200 across bench, pedestal and swing-frame types in 2026, with abrasive cost, horsepower and swing-frame reach the three largest total-cost levers for foundry buyers.
A shot sleeve is a wear part inside a magnesium die casting machine, not a competitor: sleeves meter molten Mg into the cold-chamber shot well, while the machine supplies clamping force, injection energy and cycle control. Specifying sleeve bore, material and lube protocol against the machine's shot
Vacuum die casting machine selection hinges on five engineering gates: alloy family (Al vs Mg vs Zn), vacuum level, clamping force, shot weight, and cycle-time intent. Hard vacuum (<50 mbar) is mandatory for porosity-critical structural and aerospace parts; assist vacuum (50–300 mbar) suits cosme
Gravity die casting machines in 2026 source mainly from China at US$2,100–10,000+ per ton of monthly output, with PLC + touch-screen hydraulic units and 200-ton-class monthly die-casting capacity as the dominant spec. Selection pivots on alloy (Al / Zn / Cu), mold clamp force, shot weight, and cooli
Vacuum die casting machine prices span US$8,000 for a 1-ton-class OEM precision unit to US$800,000 for a 1-piece MOQ industrial suction casting line; total project outlay is driven by chamber size, vacuum level, alloy reach, and PLC/automation tier.
A crucible furnace melts metal inside a refractory crucible — the selection pivot is charge material, melt capacity, and energy source. Pit-type, bale-out, tilting, and push-up designs are matched to alloy family, batch weight, and lift-mechanism constraints before RFQ.
Line frequency induction furnaces (line-frequency mains, typically 50/60 Hz coreless or channel units) are specified for large-tonnage ferrous melts above ~3 t per unit, where melt rate, refractory life and kWh/ton dominate the selection. Selection pivots on melt mass, alloy class, lining chemistry,
Lost foam casting lines suit short-run ferrous and non-ferrous parts from 1 kg to several tonnes where draft-free geometry and consolidated finishing offset EPS tooling cost; selection pivots on foam density (18-22 kg/m³), vacuum level (≥0.05 MPa), coating refractoriness and matched molding throughp
Core making machine selection in 2026 is decided by four production gates — binder chemistry, cycle time, sand-to-core ratio and box/pallet size — each mapping to a specific machine family: shell, hot-box, cold-box and the newer gantry core shooters.
Hot box core shooter selection turns on shot weight, platen parting plane and resin-sand cure budget. Horizontal-parting units suit manipulator take-out, vertical-parting units suit deep-draw cores above 50 kg.
Gas-fired aluminum melting furnaces and cupola furnaces serve different metals, charge profiles, and emissions regimes; specifiers must match fuel system, refractory class, and throughput before RFQ. Cupola remains dominant for cast iron, while gas-fired crucible or reverb furnaces dominate secondar
Resin sand molding lines in mid-2026 list at roughly US$5,000 per set entry-level, scaling to over US$1M for automated lines, with furan and alkali-phenolic resin, PLC control and mold size as primary cost drivers.
Sand blasting uses compressed-air-propelled abrasive for fine cleaning and finishing; shot blasting uses mechanical wheel-thrown steel shot/grit for heavy descaling. Different driving media, different surface grades, different ROI windows — pick by substrate, throughput and finish target.
Core making machines and shell core machines serve different foundry roles: general core makers cover hot-box, cold-box and shell processes in 5-200 kg shot weights, while shell core machines are purpose-built for thin-walled shell cores using heated patterns and resin-coated sand.
A 2026 Chinese-domestic crucible furnace quote spans roughly USD 1,000 for a 50 kg gas-fired aluminum-melt unit to USD 80,000+ for a 1,000 kg medium-frequency steel-melting rig; landed cost rises 18-35% over FOB once induction coils, refractory grade, freight, and CE/ISO paperwork are itemized.
Magnesium die casting machines run at 200–1200 ton clamp force with hot-chamber Mg-rated shot ends and SF6 cover-gas cells, while squeeze casting machines apply 50–150 MPa direct or indirect pressure on slow-shot metal for near-zero porosity structural parts. Choose the former for high-volume thin-w
Induction furnace selection is driven by five hard gates: melt mass per shift, target alloy class, mains frequency (line / medium / high), furnace duty (melting vs holding) and refractory life. The wrong gate pairing means 20-40% wasted kWh per ton and coil refractory turnover inside a year.
Shell molding machines in the 2026 Chinese-Fujian supply cluster span roughly US$ 90–1,380 per set, with horizontal and vertical core-shooter formats serving iron, steel and non-ferrous foundries. Selection pivots on flask size, shot weight, blow pressure, and whether a resin-shell or hot-box (shell
Drum, turntable and roller-conveyor shot blasting machines are listed between US$9,500 and US$50,000 FOB China as of June 2026, with Indian small-medium Diabola units undercutting that band; total landed cost typically runs 1.3-1.8x the ex-works price once abrasive recovery, dust collection and inst
Die casting machine buying in 2026 hinges on locking the shot-weight band first, then matching the machine class to alloy: hot-chamber for zinc, cold-chamber for aluminum and magnesium, with vacuum specified for structural castings.
Sand blasting machine selection in 2026 hinges on four hard specs: abrasive type, pressure class (40–150 psi / 3–10 bar), chamber vs open-air configuration, and dust-collection compliance. Suction units suit sub-2 hr/day workshops; pressure-pot systems dominate 8 hr industrial shifts.
Crucible induction furnaces (line-frequency 50/60 Hz coreless) and line-frequency induction furnaces (channel-type mains-frequency holders) are distinct equipment classes — not competing options. Selection hinges on duty: coreless for batch melting, channel for holding/casting flow. Lining/coil life
Vertical automatic shell core machines from Chinese foundries are listed on Goldsupplier at tier-1 volume, with Qingdao Huaxin Shengye casting-machinery offering full foundry-line packages. Sourcing routes split between 2-6 product groups on DirectIndustry and high-volume MOQ 1-ton listings on Made-
Aluminum die casting machine selection hinges on five gates: clamping force (kN/tonnage), chamber type (hot vs cold), alloy window, shot/cycle envelope, and automation class. Match the part to the press class before price.
Gas-fired aluminum melting furnaces in 2026 are typically rated 700-1250°C melt zone, 0.5-10 t/h throughput, and use refractory-fiber + fired-brick linings with PLC burner control. Selection hinges on alloy mix, NOx ceiling, and whether reverb or crucible geometry fits the foundry footprint.
Cold chamber die casting machines sized from 160T to 900T clamp force, with HS code 84543010.00, are the workhorses for aluminum and magnesium structural parts; the 2026 buying decision hinges on shot weight, tie-bar spacing, and PLC control generation rather than brand alone.
Low pressure die casting (LPDC) machine pricing spans roughly US$8,000 for small benchtop units to over US$120,000 for production aluminum wheel cells, with total project outlay driven by clamping force, shot weight, platen size, crucible capacity, and PLC retrofit scope.
Melting furnaces and crucible furnaces differ mainly in heat-source architecture and metal-handling role: a melting furnace generates heat directly to liquefy charge metal, while a crucible furnace isolates the charge in a refractory pot — a 100 kg small smelting furnace from Luoyang Ruixinsheng lis
Cold chamber die casting machine selection in 2026 hinges on four gates: alloy family (Al/Mg/Cu/Zn), shot weight envelope, clamp tonnage, and the control/HMI class — a machine specified wrong on any one gate will scrap out of gate on the rest.
Aluminum die casting machine prices in 2026 span roughly US$30,000 for a small 160-ton cold-chamber unit up to US$1,500,000+ for 1,800-3,500 tonnage presses, with total landed cost driven by clamping tonnage, platen size, servo-hydraulic controls and auxiliary systems.
Industrial melting furnace price 2026: small 500 kg medium-frequency induction units list at US$7,500–12,500 FOB China, mid-capacity 1–5 t foundry lines at US$11,600–20,500, aluminium/ferroalloy tilting furnaces at US$50,000–108,000, with 1–3 set MOQ discounts of 3–5%.
Core making machine prices span roughly US$5,500 entry-level shooting units to over US$200,000 turnkey hot-box or cold-box lines, with the binder, box size, and cycle time driving 60-80% of cost variance on 2026 quotes.
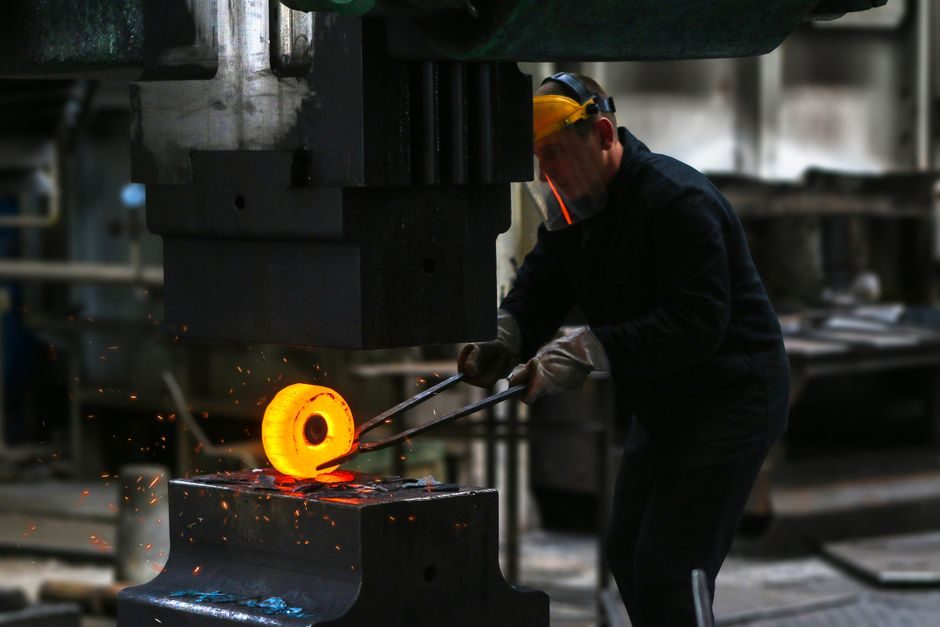
Shell core machines and hot box core shooters are two distinct core-making lines; the former uses resin-bonded sand cured in heated metal patterns (200-260°C) for thin shell cores, while hot box shoots resin sand into a heated corebox (200-250°C) for solid cores, with cycle time, core thickness, and
Industrial heat treatment furnace FOB bands in 2026 span US$3,000 handheld induction units to US$455,000 horizontal car-bottom furnaces; cost drivers are max temperature, atmosphere, capacity and refractory class.
Shell core machine pricing in 2026 spans roughly US$8,000 for entry-level Chinese semi-automatic units to over US$80,000 for European four-station CNC rigs, with the dominant cost drivers being core box size, station count, and resin-sand control package.
Medium-frequency induction furnaces in 2026 sit in a US$6,550–80,000 FOB range per set on Chinese export channels, with 0.1–3 t steel-shell variants dominating ferrous melts and 1,200 °C vacuum-chamber units covering precious-metal ingot work.
Heat treatment furnace selection in 2026 is decided by six binding spec gates: workload atmosphere, peak temperature class, quench mode, throughput geometry, footprint/utility, and certification/control scope. Batch atmosphere and sealed-quench (integral quench furnace) builds dominate alloy-steel a
High-pressure die casting machines and gravity die casting machines solve different problems: HPDC injects molten aluminium, zinc or magnesium under 30-100 MPa for thin-wall volume parts, while GDC fills brass or aluminium by tilting or hand-pour at near-atmospheric pressure for heavier sanitary and
A shot blasting machine and a sand cooler sit on opposite ends of a foundry loop: the former propels steel shot at 40–80 m/s to clean or peen castings, the latter drops return sand from roughly 300 °C to below 50 °C before moulding. Spec the wrong tool in the wrong cell and throughput, abrasive cost
A hot box core shooter uses compressed air to blow resin-coated sand into a heated core box (200–260 °C), then bakes the sand via furan/phenolic resin cure, with 2026 models sized 5–50 kg per shot and cycle times of 25–60 s for foundries.
Zinc die casting machine selection in 2026 hinges on matching hot-chamber clamp force (20–315 t), shot weight (3–3,000 g) and Z410/Z430 alloy compatibility to part geometry, then validating ISO 9001:2015 certification and CNC tie-in before pricing.
A 1-ton aluminum holding furnace on Alibaba trade channels lists in the US$10,000-30,000/set band, while 10-tonne regenerative melting-and-holding packages push lead time into the short-lead-time custom tier. Price drivers are refractory, burner or coil class, capacity, and holding temperature.
Resin sand molding line selection turns on six gates: flask size, sand throughput (t/h), mold hardness, cure time, automation level, and reclamation yield. Lines pairing furan or phenolic no-bake resin with continuous mixers and shakeout reclaim typically hit 92-95% sand reuse, while box throughput
Cold chamber die casting machines handle aluminum, magnesium and copper alloys above 660 °C melt points; zinc hot-chamber machines serve zinc and Zamak below 450 °C. Pick cold chamber for shot weights above ~1 kg or ferrous-touching alloys; pick zinc hot-chamber for sub-1 kg Zamak hardware with cycl
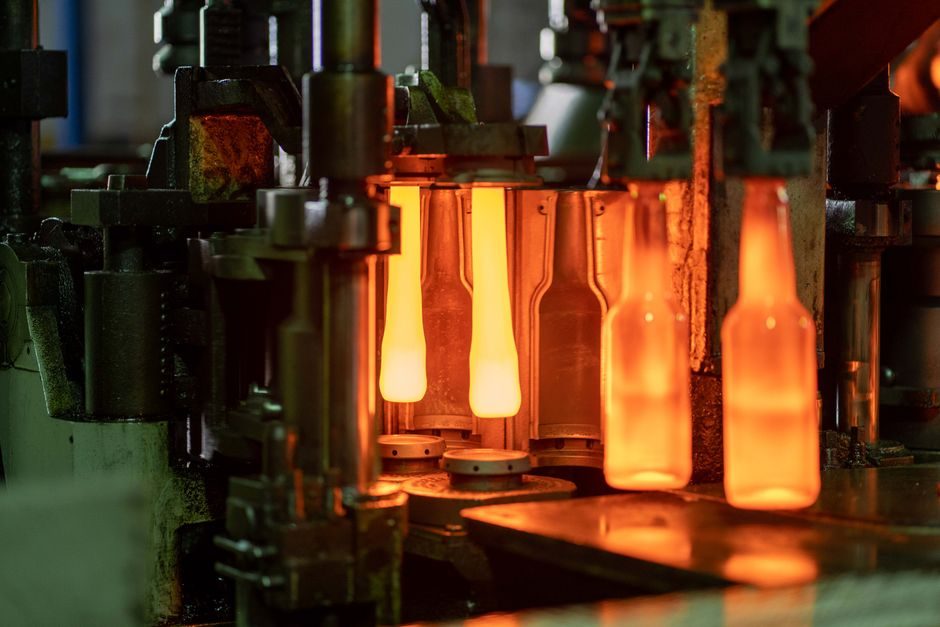
Magnesium die casting machines in 2026 span US$30,000 used hot-chamber units to US$200,000+ new 400-ton cold-chamber HPDC cells, with the metal itself at 1.8 g/cm³ the lightest structural option and the dominant cost lever being clamping tonnage and OEM brand.