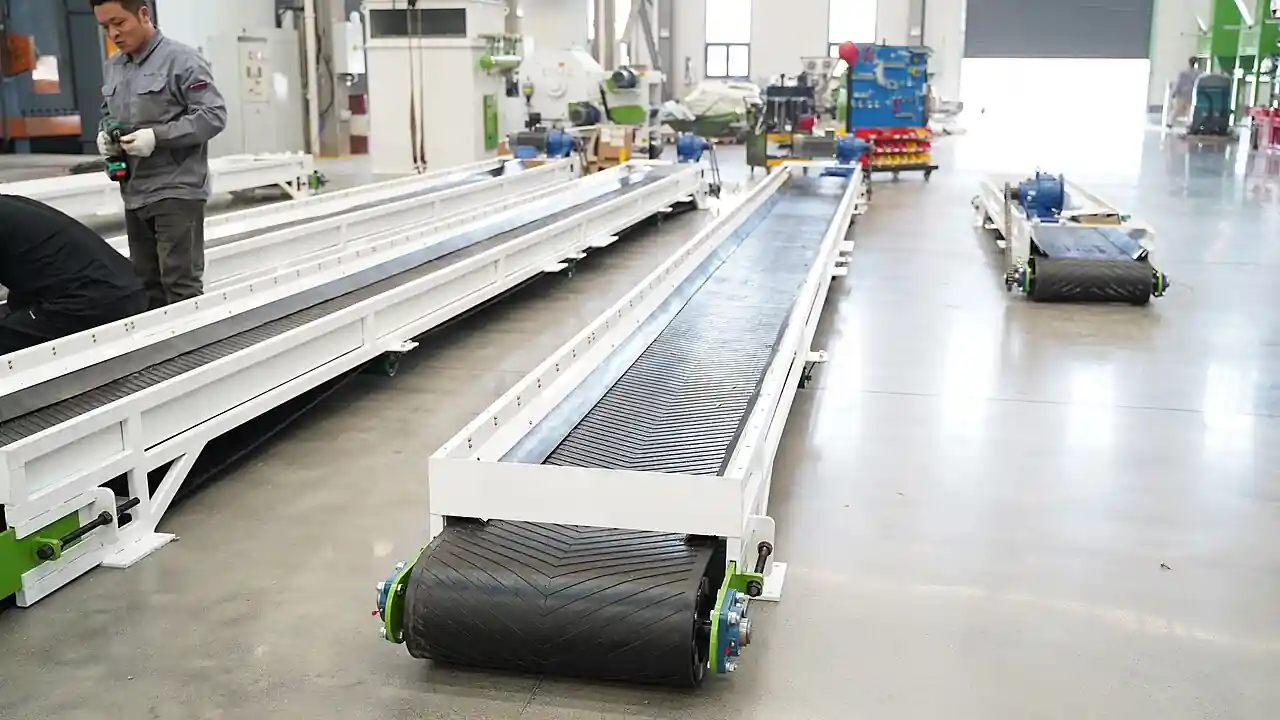
A belt conveyor is the complete conveying machine; the conveyor belt is its moving carrying component. Answer 'which type?' in two parts: choose the layout for the route and load, then the belt material and construction for the product, tension, temperature and cleaning conditions. Rubber bulk-material belting is not interchangeable with light fabric, monolithic or plastic modular belting.
The bulk-material sections below discuss rubber belting, troughing idlers, pulleys, take-up and drives, with relevant CEMA, DIN and ISO design references. That scope does not make troughing idlers or those bulk-belt standards universal requirements for light fabric, slider-bed or plastic modular systems. Specify the complete machine and the selected belt/drive arrangement together.
Use Chapter 2 to separate conveyor configurations from belt-material families. Chapters 3 and 5 explain why a belt designation such as EP500/4 is a breaking-strength classification, not a safe working-tension allowance. Confirm the complete conveyor and splice design with the selected supplier before ordering.
Chapter 1 / 06
What is a Belt Conveyor
A belt conveyor moves bulk material or unit loads continuously on an endless carrying belt. The drive, support bed or idlers, pulleys or sprockets, take-up and guarding form a system. The bulk-material sections below focus on reinforced rubber belts; light-duty fabric and plastic modular systems have different materials, drives and design requirements.
Structurally, a belt conveyor has four functional groups. First, the belt itself, a layered composite of a tension-carrying carcass (textile plies or steel cords) sandwiched between rubber covers. Second, the idler set: troughing idlers that carry the loaded top run, return idlers that support the empty bottom run, and impact idlers under the loading zone. Third, the terminal pulleys and drive: a lagged drive pulley at the head, a tail pulley, snub and bend pulleys to wrap the belt, and the drive train of electric motor, gear reducer, coupling, and backstop. Fourth, the take-up, which maintains belt tension by gravity or screw to absorb belt stretch and prevent slip at the drive.
The history of the modern belt conveyor begins in the late nineteenth century. Thomas Robins developed rubber conveyor belting for ore handling in the 1890s, and Richard Sutcliffe introduced underground belt conveyors into British coal mines around 1905, displacing rope haulage. Steel cord belting arrived in the 1940s and unlocked the long, high-tension overland conveyor. The post-war decades brought CEMA in the United States and the DIN 22101 family in Germany, which codified idler ratings, capacity tables, and power calculation into the engineering practice still used today.
The scale of belt conveying spans a wide range. Light unit-handling belts in packaging and parcel sortation run a few metres at well under one tonne per hour, while the largest overland mining conveyors move on the order of 10,000 to 40,000 tonnes per hour. The longest single-flight conveyors exceed 20 km, and conveyor systems built from many flights, such as the phosphate line in Western Sahara, extend roughly 100 km. No single belt, idler, or drive covers this range, so the engineering task is to map the duty, tonnage, lift, length, and material to a specific belt rating and idler class.
Four engineering attributes determine the quality and total cost of a belt conveyor: belt tension rating and stretch, idler bearing life, drive efficiency, and serviceability of splices and wear parts. A conveyor that is cheap to buy but under-rated on belt tension or idler class drifts, mistracks, sheds spillage, and forces frequent shutdowns to re-splice or re-bearing, so over a multi-year life the cheapest structure is rarely the lowest total cost of ownership.
Chapter 2 / 06
Conveyor Types and Configurations
Conveyor configuration and belt type are different selections. Flat, troughed, pipe and overland describe arrangement or geometry; textile, steel-cord and plastic modular describe the carrying belt. A cleat or sidewall is a feature, not a material. Specify both axes rather than using 'belt conveyor types' as one mixed list. Incline capability is duty- and design-dependent, not a universal angle limit.
Conveyor configuration
Common purpose
Condition to verify
Flat / slider-bed or roller-supported
Unit loads and suitably contained bulk loads
Product stability, support friction, transfer geometry and allowable incline.
Troughed
Bulk material carried in a formed cross-section
Belt troughability, lump size, loading/transfer design and calculated capacity.
Cleated / chevron / sidewall
Retaining a load on a rising route
Material behaviour, cleat/sidewall layout, return path and supplier's incline limits.
Pipe
Enclosed transport along a designed route
Belt pipeability, transition lengths, idler alignment and curve limits.
Overland
Long-distance route, usually bulk duty
Tension, take-up travel, terrain, starting/stopping and maintenance access.
Flat belt conveyors use a flat support bed or rollers and suit many cartons, components and packaging duties. A smooth surface does not establish a universal permissible incline: product friction, load shape, acceleration and retention features must be checked for the actual application.
Troughed belt conveyors increase the carrying cross-section by supporting the belt on angled idlers. Trough angle, belt troughability, load support, transitions and minimum pulley geometry must be compatible. Do not infer that a steel-cord or fabric belt can use a particular trough angle solely from its reinforcement family; verify the actual belt design.
Cleats, chevrons and sidewalls help retain material on rising routes, but their usable angle depends on the material and the complete belt/return design. Pipe conveyors enclose the load in a specially designed belt formed by idlers; suitability for a curved route requires a supplier's transition and curvature design, not simply a cover-grade choice.
Overland conveyors are long single-flight troughed conveyors, often kilometres long, engineered to follow terrain with horizontal and vertical curves and frequently driven by multiple pulleys with controlled starting. They replace fleets of haul trucks on mine-to-port and quarry-to-plant routes, cut diesel use and emissions sharply, and almost always use steel cord belting for the high tension and low stretch that long runs demand.
Chapter 3 / 06
Belt Carcass and Cover Construction
The following two rubber-belt carcass families serve bulk-material duty. They are not a complete list of every conveyor belt. For unit handling or processing, separately consider fabric-based belts with suitable covers and plastic modular belts. Habasit's fabric-belt guide discusses cover and tension-member selection; its modular-belt overview describes interconnected plastic modules.
Belt construction / material
Selection context
Do not infer
Fabric-based belt with a selected polymer cover
Unit handling or processing; cover chosen for release, wear, cleaning and product compatibility
That every fabric belt is a rubber bulk-material belt or uses an EP rating.
Rubber-covered textile carcass
Bulk duty needing the selected tensile strength, impact resistance and splice arrangement
Safe working tension directly from the designation number.
Rubber-covered steel-cord carcass
Duties where the calculated tension, stretch and route favour steel-cord construction
A universal crossover length or an automatic replacement for a fabric belt.
Plastic modular belt
Unit handling / processing with modules and a matched drive system
The same pulley, take-up and tension rules as a friction-driven rubber belt.
Property
Textile (EP / NN)
Steel cord (ST)
Designation example
EP500/4
ST2500
Nominal strength designation (not allowable working tension)
EP80 to ~EP2000 N/mm
ST630 to ST6300 N/mm
Elongation at rated load
~1.5 to 4%
<0.25%
Relative weight
Light
Heavy
Min. pulley diameter
Smaller
Larger
Splice method
Hot or cold step splice
Vulcanised cord splice
Typical duty
Short to medium, moderate tension
Long overland, steep, high tonnage
EP500/4 describes the textile carcass, not its allowable service tension. EP denotes polyester/polyamide reinforcement; 500 is the nominal full-belt longitudinal tensile strength at break in N/mm, and 4 is the number of plies. It is not '500 N/mm working tension at 10% of breaking strength'. Fenner Dunlop's explanation of multi-ply classification identifies the strength-at-break and ply-count axes, and its EP630/4 example illustrates overall strength across all plies. Permissible operating tension must come from the belt/splice design, duty and supplier's design factors.
Steel-cord belts use longitudinal steel cords rather than textile plies. Confirm the selected ST designation and nominal breaking-strength basis with the manufacturer's specification; do not treat the number as allowable operating tension. Tension, elongation, splice efficiency, pulley diameter, troughability and take-up requirements must be assessed together. There is no universal EP1600 cut-off at which all fabric belts should be replaced with steel cord.
Cover grades set the abrasion and cut resistance of the rubber and are tested to ISO 4649, formerly DIN 53516, by measuring rubber volume loss against an abrasive sheet on a rotating drum. Two parallel grade systems are in use. DIN 22102 uses grade Y for normal service, grade W for high abrasive wear with low volume loss, and grade X for very high abrasion plus the best cut, gouge, and impact resistance for sharp or heavy lump. EN ISO 14890 uses grade L (normal, equivalent to DIN Y), grade D (high abrasion, equivalent to DIN W), and grade H (best all-round, equivalent to DIN X). Carrying cover thickness typically runs 2 to 8 mm and the running cover 2 to 6 mm, set by drop height and abrasiveness. The table below maps common service conditions to a starting cover grade.
Service condition
DIN 22102 grade
ISO 14890 grade
Normal abrasion, low drop
Y
L
High abrasion, fine to medium material
W
D
Sharp, heavy lump, high drop height
X
H
Underground / fire-risk (flame, antistatic)
K grade (DIN 22131)
EN 12882 / EN 14973
Beyond abrasion grade, special compounds tailor the belt to the medium: oil and grease resistant covers for oily ore and recycling, heat resistant covers for sinter and clinker, and flame-resistant antistatic covers for underground coal and enclosed plant. Fire and static safety is governed by ISO 340 and ISO 284, with the European framework EN 12882 and the underground grade EN 14973, succeeding the former German K grade defined in the DIN 22131 and DIN 22102 family. Specifying a flame-resistant belt is a regulatory requirement, not a preference, in coal mines and many enclosed conveyors.
Chapter 4 / 06
Idlers, Pulleys, Drives, and Standards
Below the belt sit the components that carry it, drive it, and keep it tracking. Their ratings come from CEMA in North America and the DIN and ISO families internationally, and getting them right is what separates a conveyor that runs for years from one that mistracks and sheds spillage from the first week. This chapter covers idlers, pulleys, the drive train, take-up, and the standards that bind them together.
Idlers are the rotating rollers that support the belt. A troughing idler station has three rolls: a horizontal centre roll and two wing rolls set at the troughing angle. CEMA rates idlers by duty class from light to heavy, designated CEMA B, C, D, E, and F, with each class tied to belt width and roll diameter. CEMA B idlers suit belt widths from roughly 18 to 48 inches with 4 and 5 inch roll diameters, while CEMA E and F idlers cover the widest belts, from 36 to 96 inches and 42 to 120 inches respectively, on heavy-duty mining conveyors. CEMA Standard 502 covers bulk-material troughing and return idlers. Under the loading point, cushioned impact idlers absorb the energy of falling material, and self-aligning idlers correct belt drift.
Pulleys terminate and steer the belt. The drive (head) pulley transmits motor torque to the belt by friction and is lagged with rubber or ceramic to raise the friction coefficient and shed wear. The tail pulley returns the belt at the loading end, while snub and bend pulleys increase the wrap angle around the drive to improve traction. The minimum pulley diameter is set by the belt carcass: stiffer steel cord and thicker textile belts need larger pulleys to avoid fatigue in the splice and carcass, which is why upgrading a belt rating can force a pulley change.
The drive train couples an electric motor to the drive pulley through a gear reducer and coupling, with a backstop or brake to prevent rollback on inclined conveyors. The table below lists the principal standards a buyer references when specifying and rating a belt conveyor system.
Standard
Scope
CEMA, Belt Conveyors for Bulk Materials
Capacity tables, idler classes, power and tension (North America)
DIN 22101
Belt conveyor design, drives, brakes, take-up, power and tension
ISO 5048
Operating power and tensile force calculation, idler conveyors
DIN 22102 / EN ISO 14890
Textile (EP) belt construction and cover grades
DIN 22131 / ISO 15236
Steel cord belt construction (ST630 to ST6300)
ISO 433 / ISO 4649
Belt marking; cover abrasion test method
ISO 340 / ISO 284 / EN 12882
Flame resistance, antistatic, and safety of belts
ASME B20.1
Safety standard for conveyors and related equipment (US)
Power and tension are calculated by ISO 5048 and DIN 22101 by summing the resistances to motion. The main resistance comes from idler rotation and the flexing of belt and material, expressed through a friction factor f near 0.020 to 0.030 applied to the moved mass and length. To this the calculation adds the lift resistance from any change in elevation, the secondary resistances at loading and skirting, and special resistances from plows or trippers. The effective tension at the drive multiplied by belt speed, divided by the drive efficiency, gives the required motor power. CEMA reaches the same result with separate friction coefficients for idlers, belt, and material rather than one global friction factor, and the two methods agree within a few percent on most conveyors.
The take-up maintains the minimum tension needed to prevent slip at the drive and to limit belt sag between idlers. A gravity take-up hangs a weighted bend pulley on the return run and self-adjusts to belt stretch and temperature, which is preferred on long conveyors; a screw take-up is a manually adjusted threaded frame used on shorter conveyors. Controlled-start drives, using fluid couplings or variable frequency drives, ramp the belt up gradually to keep starting tension within the belt and splice rating, which matters most on long, heavily loaded inclined conveyors.
Chapter 5 / 06
Key Specification Parameters
Reading a conveyor and belt spec sheet is a core procurement skill. A tender may list dozens of parameters, but a smaller set drives the selection: belt width, belt speed, capacity, belt tension rating, troughing angle, conveying length and lift, drive power, and cover grade. Each is explained below.
Belt width is the dominant dimension and should be chosen from a standard series so idlers, pulleys, and belts are available off the shelf. The common metric series is 500, 650, 800, 1000, 1200, 1400, 1600, 1800, 2000, 2200 mm, and the CEMA imperial series runs 18, 24, 30, 36, 42, 48, 54, 60, 72, 84, 96 inches. Width must also clear the maximum lump size: a practical rule keeps the largest lump below about one third of the belt width so material centres on the belt and does not jam at skirts or chutes.
Belt speed trades capacity against wear and spillage. For coal, grain, and sand, 2 to 4 m/s is typical; for large or sharp lump that would damage the belt or bounce off, speed is held to roughly 1.5 to 3.5 m/s; and only fine, light, non-abrasive material on wide overland belts runs at 6 to 8 m/s or more. Higher speed lifts throughput on a given width but raises idler bearing wear, belt cover wear, dust generation, and the energy lost to material turbulence at transfer points.
Capacity, in tonnes per hour, is the product of the belt cross-sectional load area, the belt speed, and the material bulk density. The load area is fixed by belt width, troughing angle, and the material surcharge angle, the angle at which loose material heaps above the trough, and is read directly from CEMA or ISO 5048 capacity tables. Because capacity scales with both area and speed, a modest width increase or a deeper trough often beats simply running the belt faster.
Breaking strength and working tension must be kept separate. The EP/ST strength designation characterizes the belt; the conveyor calculation provides service tensions, including starting and stopping. Select the carcass and splice using the applicable design method and supplier's permissible-tension data. Do not compare calculated peak tension directly with EP500/4's 500 N/mm, and do not apply one generic safety factor to every belt or splice.
Troughing angle (20, 35, or 45 degrees) sets how deep the belt folds and therefore the load area, but a deeper trough demands a more flexible belt that can conform without edge buckling, which limits how steeply a stiff or steel cord belt can be troughed. Conveying length and lift drive the tension and power: length sets the main rolling resistance, while lift sets the potential energy added to or recovered from the load. Drive power is the motor rating sized from the ISO 5048 or DIN 22101 calculation plus margin.
Two further parameters round out a complete specification:
Cover grade and thickness: DIN Y/W/X or ISO L/D/H abrasion grade with carrying and running cover thickness, set by drop height and abrasiveness as covered in Chapter 3.
Environmental and safety class: flame-resistant and antistatic rating to ISO 340 and ISO 284 for underground and enclosed duty, plus ingress and temperature limits, guarding to ASME B20.1, and pull-cord and belt-drift switches.
Chapter 6 / 06
Selection Decision Factors
To turn the preceding chapters into a specified machine, follow the decision sequence below. Most selection mistakes come not from a single wrong number but from deciding a downstream parameter, such as belt rating, before the upstream ones, such as material and tonnage, are fixed. These eight steps form a reusable RFQ template.
Material and tonnage: Define the bulk material, its density, lump size, abrasiveness, moisture, temperature, and the required throughput in tonnes per hour. These set every downstream choice, from cover grade to idler class.
Geometry, length and lift: fix the route, vertical change, transfers and curves. Confirm load retention and permissible incline from the selected material/belt system rather than treating angle of repose as an operating limit.
Belt width and speed: Choose a standard width that clears the maximum lump (lump below about one third of width), then set belt speed from the material class so capacity meets tonnage without excess wear, dust, or spillage.
Belt carcass and rating: calculate service and transient tensions, then select carcass, splice and take-up using the applicable design method and supplier's allowable-tension guidance. Nominal breaking strength is not working tension; EP1600 is not a universal fabric/steel-cord crossover.
Cover grade and special compounds: Select the abrasion grade (DIN Y/W/X or ISO L/D/H) and cover thickness for the drop height and abrasiveness, and add oil, heat, flame-resistant, or antistatic compounds where the medium or location requires them.
Idlers, pulleys, and structure: Choose the CEMA idler class for width and load, the troughing angle compatible with the belt, the minimum pulley diameters for the carcass, impact and self-aligning idlers at loading, and the frame or trestle structure.
Drive, take-up, and controls: Size the motor from the power calculation, select the gear reducer and coupling, add a backstop on inclines, choose gravity or screw take-up, and specify controlled starting (fluid coupling or VFD) on long or heavily loaded conveyors.
Total cost of ownership (TCO): Sum capital, installation, energy, and the recurring cost of belt replacement, splices, idler bearings, and cleaning. A belt or idler chosen on lowest first cost but high wear or drift can cost more in downtime and spillage within a few years than the premium for the correctly rated part.
One last dimension is often overlooked at the purchasing stage but decides repair response over a 10 to 20 year life: manufacturer serviceability. Local availability of splice crews and vulcanising kits, off-the-shelf replacement belts in the chosen width and rating, idler and pulley spares, and field engineering support all determine how fast a stopped conveyor returns to service. Established system and belt suppliers such as FLSmidth, Metso, BEUMER, Sandvik, Continental ContiTech, Fenner Dunlop, and Bridgestone maintain engineering and after-sales networks across major mining and bulk regions, which makes them dependable choices for large projects where downtime is the dominant cost.
FAQ
What is the difference between a belt conveyor and a conveyor belt?
A belt conveyor is the complete machine; a conveyor belt is its carrying component. An RFQ for the machine must state route, throughput, material, transfers, drive, support and safety scope. An RFQ for the replacement belt must state construction, width, strength designation, cover, splice and required compatibility. Rubber bulk-material belts, fabric processing belts and plastic modular belts are not interchangeable merely because all are called conveyor belts.
How do I read a belt designation like EP500/4 or ST2500?
EP500/4 identifies a polyester/polyamide textile carcass with a nominal overall longitudinal tensile strength at break of 500 N/mm and four plies. The number is not allowable working tension, and it must not be described as 10% of the breaking strength. For an ST designation, confirm the steel-cord belt's nominal strength and full ordering specification with its manufacturer. Choose permissible operating tension through the belt and splice design, including the applicable design factors and transient loads.
What do the cover grades W, X, Y, H, D, and L mean?
Cover grade sets the abrasion and cut resistance of the top and bottom rubber, tested to ISO 4649 (DIN 53516). Two parallel systems exist. DIN 22102 uses Y for normal service, W for high abrasive wear with low volume loss, and X for very high abrasion plus the best cut, gouge, and impact resistance for sharp or heavy lump. EN ISO 14890 uses L (normal), D (high abrasion, equivalent to DIN W), and H (best all-round resistance, equivalent to DIN X). Carrying cover thickness typically runs 2 to 8 mm and the running cover 2 to 6 mm. Match the grade to drop height, lump sharpness, and abrasiveness, not to a generic catalogue default.
How do I size belt width and speed for a target throughput?
Capacity is the product of cross-sectional load area, belt speed, and bulk density. The load area is fixed by belt width, troughing angle (20, 35, or 45 degrees), and material surcharge angle, and is read from CEMA or ISO 5048 capacity tables. Pick a standard width (500, 650, 800, 1000, 1200, 1400, 1600, 1800, 2000 mm, or the 18 to 96 inch CEMA series) so idlers and belts are off the shelf. Then set speed: 2 to 4 m/s for coal, grain, and sand, 1.5 to 3.5 m/s for large or sharp lump to limit belt wear and spillage, and up to 6 to 8 m/s only for fine, light, non-abrasive material on wide overland belts. Keep lump size below one third of belt width.
How is conveyor drive power calculated?
ISO 5048 and DIN 22101 calculate the effective tension at the drive pulley by summing the resistances to motion: the main resistance from idler rotation and belt and material flexing (a friction factor f near 0.020 to 0.030 times the moved mass and length), the lift or lower resistance from the vertical change in height, the secondary resistances at loading and skirting, and any special resistances such as plows and trippers. Drive power equals effective tension times belt speed, divided by the drive efficiency. CEMA reaches the same result with separate friction coefficients for idlers, belt, and material rather than one global f, so the two methods agree within a few percent on most overland conveyors.
When should I choose a steel cord belt over a fabric EP belt?
Choose from calculated tension, permissible stretch, route, take-up, pulley sizes, impact, splice capability and maintenance conditions. Steel cord often suits high-tension, low-stretch duties, but it is not automatically best above one length or EP rating. A suitable fabric construction may offer different impact, troughing and repair advantages. Compare the manufacturer's permitted operating conditions and splice design, not just nominal breaking strength.
What standards and safety rules govern belt conveyors?
Design and rating sit on CEMA Belt Conveyors for Bulk Materials (North America), DIN 22101 and ISO 5048 for power and tension, and the idler and belt standards DIN 22102, DIN 22131, ISO 433 marking, and EN ISO 14890. Underground and fire-risk duty requires flame-resistant and antistatic belts to ISO 340, ISO 284, EN 12882, and EN 14973, and the former DIN K grade. Machine safety follows EN 620 and EN ISO 12100 family practice plus regional rules: the EU Machinery Regulation 2023/1230 (replacing Directive 2006/42/EC), and in the United States ASME B20.1 Safety Standard for Conveyors and Related Equipment. Nip-point guarding, pull-cord stops, and belt-drift switches are mandatory protective measures.