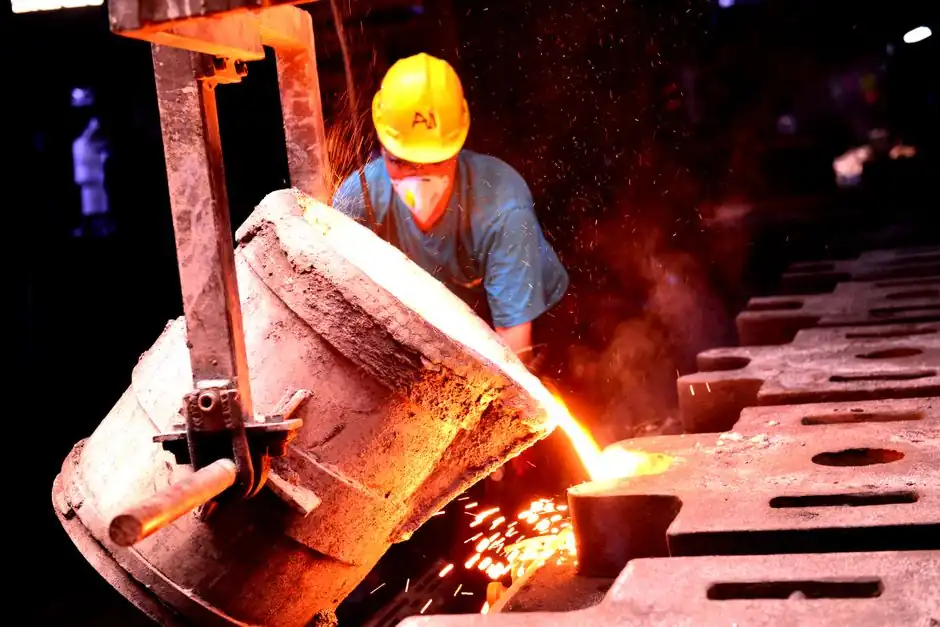
A 2026 procurement audit for large aluminum die castings collapses into four evidence classes: QMS registration, sector-specific accreditation, market-access safety marks, and machine-floor capability proof, with IATF 16949:2016 and ISO 9001 treated as non-negotiable for automotive and regulated-industry buyers [S1][S3].
The decision matters because large structural castings (battery housings, motor cases, transmission housings) carry mechanical, pressure-tightness, and traceability loads that commodity castings do not. A supplier who passes an ISO 9001 desktop review can still fail a Tier 1 PPAP if the machine list, alloy traceability, and process-monitoring evidence do not line up with the part's risk class [S2][S4].
Certification Stack: QMS, Sector, and Market-Access Marks
ISO 9001:2015 is the baseline, with IATF 16949 added for automotive Tier 1 programs and AS9100 required when castings feed aerospace or defense assemblies, per supplier-side audit guidance from August 2026 [S3][S7]. The 2026 North American supplier landscape confirms IATF 16949:2016 and ISO 9001 as the floor for any shortlist feeding OEM structural programs [S1]. For buyers shipping into Europe, North America, or Australia, the same supplier must also hold the destination market's safety marks: CE for the EU, UL or ETL for North America, SAA for Australia, and equivalents as listed in the supplier's audit pack [S3].
Verification path: ask for the certificate number, the issuing CB name, the accreditation body (e.g. UKAS, ANAB), the original issue date, and the surveillance or recertification expiry. Cross-check the scope statement line by line against the part family you are sourcing; an IATF 16949 certificate that excludes "high-pressure die casting of structural aluminum components" does not cover your program. AS9100 scope must explicitly include the aerospace part numbers or process families on the audit you are sourcing [S4]. For the underlying die casting machine capability, a certificate alone is not enough, since the QMS scope can be valid while the physical press is not in the scope of accreditation.
Machine Capability Proof: Tonnage, Alloys, and Process Windows
Large aluminum castings need clamping force matched to projected area and shot weight, with credible supplier programs running 60T to 2,500T clamp coverage and explicitly listing high-tonnage presses for structural parts [S1]. A credible supplier publishes a machine list with make, model, clamp tonnage, and shot sleeve capacity; one example North American shop runs 12 machines from 250T to 1,600T, including a 1,600T Buhler Carat and a 1,600T Prince for large structural work [S5].
For large thin-walled NEV housings, ask which presses are allocated to the program and confirm shot weight plus platen dimensions can hold the part with the required shot-to-casting ratio. Alloys in the audit pack should cover the high-volume aluminum family (A356, A380/ADC12, 383, 384, 390, 413) and any project-specific grade, with the supplier naming the actual standard referenced for chemistry limits (ASTM, EN AC-xxxxx, or JIS H 5302) [S4][S5]. For vacuum die casting work on pressure-tight housings, ask for documented vacuum levels, leak-rate test data on first-articles, and the process-monitoring logs (Visi-Trak, MAGMA simulation outputs) used to lock the process window [S5].
Process Control and Non-Destructive Test Evidence
Foundries running 18 to 22 process checkpoints, from alloy verification at the furnace to final dimensional inspection, produce auditable evidence at every stage, and the leading tier adds X-ray tomography and ultrasonic scanning for sub-surface flaws on safety-critical parts [S4]. Coordinate measuring machine (CMM) data on production runs should hold roughly ±0.15 mm tolerance on about 97% of features, the level typically expected for sealed mating surfaces on EV battery enclosures [S4].
IoT and machine-learning monitoring on injection cells is now common at the top tier: roughly 3,000 process data points per hour per cell, with anomaly detection flagging shot-speed or intensification-pressure drift before the casting escapes the cell [S4]. For the supplier's aluminum die casting machine line, ask for the monitored parameter list (intensification pressure, slow-shot to fast-shot transition, die-spray volume, cooling-water inlet/outlet delta-T, cycle time histogram) and the alarm thresholds, then tie those to the part's control plan. ASM International data cited in 2024 attributes roughly three out of four casting defects to mould design or solidification, so suppliers should present solidification simulation runs (MAGMA, ProCAST, FLOW-3D) on the actual part geometry, not generic examples [S4].
Material and Heat-Treatment Specification for Large Structural Castings
For NEV motor and battery housings, A356 (AlSi7Mg) is the dominant alloy, with 6 to 12% Si for filling and reduced shrinkage, 0.25 to 3% Mg for Mg₂Al₃ precipitation strengthening, Cu held to 0.5 to 3.2%, and combined Pb+Sn capped at 0.05% to limit hot-cracking risk [S2]. The standard delivery condition for high-demand applications is A356-T6, achieved by solution treatment at 535±5 °C for 6 to 12 hours followed by artificial aging at 155 °C for 3 to 6 hours, raising typical tensile strength from 200 MPa to 280 MPa, with a procurement floor usually set at 310 MPa tensile for safety-critical housings [S2].
Dimensional accuracy on critical mounting surfaces should be specified to CT6 to CT8 per GB/T 6414, with the supplier's PPAP pack showing actual CMM reports on first-articles and a capability index (Cpk ≥ 1.33 is the typical automotive target) on key features [S2]. For buyers comparing process routes, low-pressure casting and gravity die casting offer lower gas entrapment and porosity than conventional high-pressure die casting, useful for housings with 3 to 5 mm walls and 6 to 7 mm embedded cooling channels, but at a higher cycle-time cost [S2][S3].
Five-Criteria Comparison Across Supplier Options
Buyer-side evaluation frameworks published in 2026 cluster around five criteria: alloy capability, machine capacity, certifications, industry track record, and post-casting service depth, and a supplier who scores on all five is a credible shortlist candidate [S1]. The decision table below lines up the main supplier archetypes against the four audit gates that matter for large structural castings:
1) Tier 1 automotive die caster (IATF 16949:2016, AS9100 on demand, 800 to 2,500T presses, in-house NDT): strongest fit for NEV housing and transmission programs; longest lead time for new tooling; highest price per casting; full PPAP support [S1]. 2) General industrial aluminum job shop (ISO 9001:2015 baseline, 250 to 1,600T presses, 360/380/390/413 alloys, squeeze-pin and vacuum-assist options): best fit for non-safety-critical housings, enclosures, and prototypes needing fast iteration; Cpk and IATF scope must be verified per program [S5]. 3) Offshore specialist (IATF 16949 plus CE/UL/ETL/SAA, large-tonnage presses, in-house machining): viable for cost-down programs, typically 25 to 40% lower landed cost than equivalent US supply, but requires direct-mill auditing, container-level inspection, and verified alloy traceability [S1][S3]. 4) Integrated magnesium die casting machine line (multi-alloy, 60T to 2,500T, IATF 16949): only worth specifying when the lightweighting target requires Mg, since the safety, melt-handling, and flux-chemistry evidence demands are heavier than for aluminum.
Audit Failure Modes and How to Catch Them
The most common 2026 audit failures, in order, are: certificate scope narrower than the part family; IATF 16949 certificate held by the trading company rather than the producing foundry; market-access marks (CE/UL/ETL) listing the wrong part number or test standard; machine list not matching the tonnage range cited in the supplier brochure; and NDT evidence limited to first-article with no ongoing production sampling [S3][S4]. A second-tier failure is the zinc die casting machine or aluminum cell running without a calibrated load cell on the shot, so intensification pressure cannot be proven part-to-part, which kills the PPAP for any safety-critical housing [S4][S6].
To verify, demand the on-site audit report from the certification body, not just the certificate PDF, and read the scope exclusions, the non-conformities, and the closure dates. For each large press allocated to the program, request a current calibration record for the tie-bar strain, the shot-end position, and any vacuum transducer, then tie those to the process-monitoring data the supplier will hand over at PPAP [S5][S6]. Treat the industrial solvent certification checklist approach as a useful analogue: same evidence ladder (scope, calibration, traceability, surveillance), different commodity.
Trackable signals to watch: (a) whether the supplier's IATF 16949 surveillance audit closed clean in the past 12 months, with the audit report number on file; (b) whether the AS9100 scope explicitly names "high-pressure aluminum die casting" rather than only "investment casting" or "machining"; and (c) whether the CE/UL file for the destination market references the standard matching the part's risk class. These three checks, applied before tooling PO, separate the structural-casting shortlist from the commodity-casting inbox.