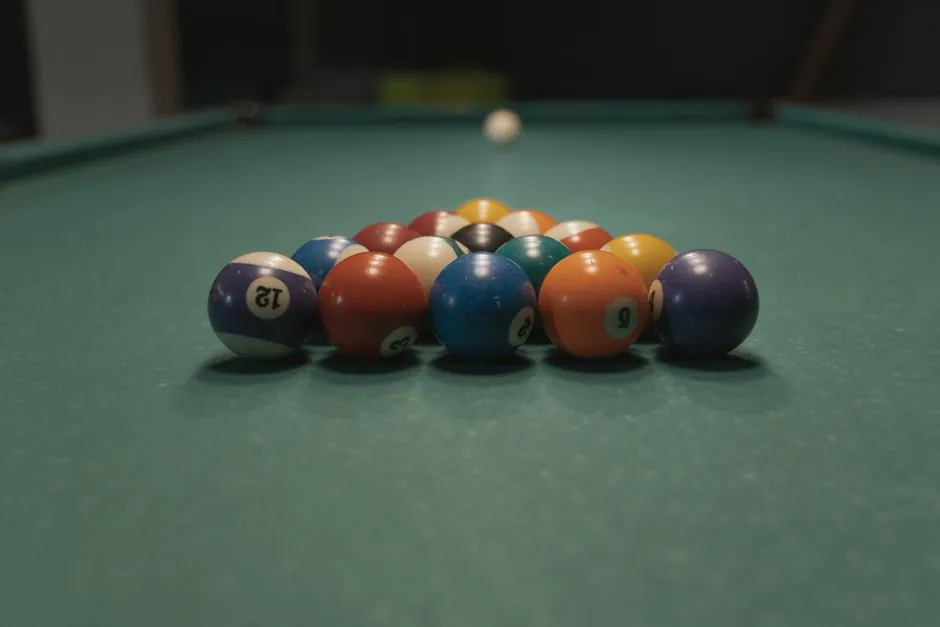
A linear guide block with a ball retainer (cage) spaces the recirculating balls at fixed pitch, eliminating ball-to-ball contact and holding the train in place when the block is removed from the rail [S1][S2]. A full-complement (non-caged) block packs the maximum number of balls into the load zone, with no plastic or metal separator between them [S1][S2].
The trade-off is consistent: retainers remove a small amount of load-carrying steel from the circuit but cut friction, noise, and lubricant starvation. Full-complement designs do the opposite. Selecting between them is one of the highest-leverage decisions in sizing a profile-rail linear guide carriage, because the same block housing can ship in either configuration from most major suppliers [S3].
How the Ball Retainer Changes Block Mechanics
In a conventional recirculating block the balls are in line contact with each other at the curved turnaround inside the end caps, and the contact patch is a near-point load running at roughly twice the linear speed of the ball train [S2]. A retainer converts that interface into a distributed contact between the ball OD and a pocket in the cage, dropping the Hertzian surface pressure and the heat that goes with it [S2]. NTN's published explanation is explicit: the cage in caged linear guides acts as a retainer preventing contact between the balls, and the larger contact area (A) reduces the surface pressure (P) leading to less heat generation and longer life [S2].
Retainers also fix the ball-to-ball pitch (C1, C2) along the circuit, which a non-caged block cannot do because the balls ride directly on each other [S2]. Fixed pitch smooths motion, and it gives the cage pockets a controlled geometry to hold grease reservoirs, a benefit NTN documents as lubricant storage gaps in the cage structure [S2]. Misumi's field guidance makes the practical case in one line: the balls are retained with a ball retainer; this is very important because if balls fall out, this will cause an uneven loading condition in the block and can lead to catastrophic failures over time [S1].
Load Capacity, Speed, and Noise: the Real Numbers
No OEM in the supplied sources publishes a single percent for the load penalty of a caged block, but the directional facts are consistent and quotable. Caged designs intentionally reduce the number of load-carrying balls in the raceway to make room for the cage pockets, so the basic dynamic load rating (C) of a caged block is lower than the same block in full-complement form, while the static rating drops less because preload and contact angle are unchanged [S2][S3]. Where the caged geometry clearly wins is on the parasitic losses: cage pockets separate adjacent balls, so friction, acoustic emission, and grease churn all fall, and the noise level is reduced through the structural flexibility of the cage [S2].
For a sense of the surrounding component envelope, PBC Linear's published plain-versus-ball comparison table shows a ball-bearing linear block rated to about 2,165 lb (9,630 N) static load and roughly 590 SFM (3 m/s) maximum speed, always with lubrication, against a plain-bearing alternative that goes to 100,500 lb (447,046 N) static and 825 SFM (4.19 m/s) with lubrication [S5]. Those numbers are not the caged-vs-full-complement delta, but they bracket the operating window a profile-rail designer is usually working inside, and they underline why full-complement profile-rail blocks are still specified whenever the absolute highest load per block size is required [S4][S5]. NSK's own overview ties the same point to speed and contact angle: the ball is proportional to the speed of the linear guide, and the contact angle determines the loading capacity of the linear bearing [S6].
Selection Criteria: When to Pick Caged, When to Pick Full Complement
Use this five-criterion matrix when choosing between a caged and a full-complement block of the same housing size. Values are qualitative where the sources are qualitative, with the [S#] that supports each claim. [S3]
1. Peak load per block. Full complement wins. More steel balls in the load zone raises the basic dynamic rating C for the same block geometry [S2][S3]. Caged blocks accept a smaller C in exchange for smoother running and lower heat [S2].
2. Maximum travel speed. Caged wins. Eliminating inter-ball contact roughly halves the contact-point surface speed inside the recirculator, which is the dominant speed-limit mechanism in many profile-rail blocks [S2][S6].
3. Noise and cleanliness. Caged wins by a wide margin. Caged blocks are commonly used in high-speed or high-precision equipment, semiconductor and medical clean rooms, and any application where sound pressure is metered [S2][S3].
4. Lubrication interval. Caged wins. Cage pockets hold grease reservoirs, lengthening the interval between re-lubes; conventional blocks rely on the balls picking up oil from the raceway, so lube life is shorter [S2].
5. Maintenance and field handling. Caged wins for block-on-rail removal, full-complement requires a fixture or a careful hand. With a caged block the balls stay in the block when it is pulled off the rail [S1][S2]; without a cage, balls fall out and the load becomes uneven, which can lead to catastrophic failures over time [S1]. Field threads on reassembly are full of exactly this failure mode: how to put balls back inside bearing block in a non-caged block and get it back on the rail without knocking them out again [S9].
Compatibility, Interchangeability, and Drop-In Risk
Retainer versus no retainer is a block-side decision, not a rail-side decision, and that matters for retrofit work. NTN's published "One Rail For All" approach runs both conventional and caged runner blocks on the same rail, meaning no reassembly of the guide rails is required in changeover situations [S2]. HIWIN's HG series block is also built to be freely paired with any rail of the same series while retaining dimensional accuracy, with a ball retainer integrated into the block to keep the steel balls in place when the carriage is removed for maintenance [S3].
The compatibility question the field actually asks, though, is whether a caged block can be swapped onto a rail that was previously running full-complement blocks of the same part number. The two answers in the research are: yes if the supplier publishes the rail as common to both variants (NTN's approach [S2]), and yes-with-check if the supplier publishes the block as interchangeable across the series (HIWIN's HG approach [S3]). What is not supported by the sources is mixing caged and full-complement blocks on the same axis simultaneously, because their preload behaviour, friction, and stick-slip differ enough to skew parallelism and cause uneven loading [S1][S2].
Failure Modes and Limits to Watch
Full-complement blocks fail in three repeatable ways. First, balls drop out during block removal, the load becomes uneven, and the block wears in a wave pattern that the user notices only after thousands of cycles [S1][S9]. Second, starved lubrication at the ball-to-ball turnaround in the end cap generates heat that accelerates grease degradation [S2]. Third, higher inter-ball friction translates directly to higher running temperature at speed, which on long-stroke, high-duty cycles is the limit that matters before the basic dynamic rating does [S2][S6].
Caged blocks fail differently. Cage-pocket wear or pocket cracking at high speed changes the ball-pitch spacing, and once that spacing drifts, smoothness and noise performance degrade even though load rating is largely unaffected. The cage is also a plastic or polymer component with a temperature ceiling well below the steel raceway, so any application pushing block temperature past the cage rating will see the cage fail before the steel does. The two failure modes are not equivalent: full-complement failures usually look like accelerated raceway wear, caged failures usually look like a cracked, melted, or worn cage and a sudden change in noise signature.
Use Cases Drawn From the Research
Clean-room semiconductor and medical assembly: caged. The noise and particulate benefits of a cage, plus the longer lube interval, dominate the small loss in basic dynamic load rating [S2][S3].
Heavy machine-tool axis, large gantry, press ram: full-complement. Maximum load per block envelope is the constraint, and the higher running temperature is acceptable because duty cycle and ambient are controlled [S2][S4].
3D printer head, optical bench, laboratory automation, metrology stage: caged. Smoothness at low speed, quiet operation, and the ability to lift the carriage off the rail for service without losing balls all matter more than the last few percent of load rating [S1][S2][S3].
High-cycle packaging or indexing line running 24/7: caged, primarily for the lube-interval win. NTN's published explanation is that, with the cage, the balls are continuously supplied with lubricant, which reduces wear of the metal and significantly extends the service life of the lubricant and the maintenance intervals [S2].
Field service kit for any profile-rail machine: caged. The retainer is the difference between a 30-second block swap and a 30-minute ball-recovery job, and that operational reality shapes the recommendation every time [S1][S9].
Engineering Specs and Standards Anchors
Profile-rail linear guides are commonly classed under ISO 14728 (rolling bearings, linear motion rolling bearings, Part 1 for ball slides, Part 2 for roller slides), which defines how the basic dynamic load rating C, the basic static load rating C0, and the frictional drag are calculated; the caged-versus-full-complement distinction is captured inside the part-1 load-rating formulas as a reduction factor on the ball count in the load zone. For preload class and accuracy, ISO 14728 works alongside the older JIS B 1192-1991 / B 1194-1996 framework that HIWIN, THK, NSK, and others still publish against; preload classes Z0, Z1, Z2, Z3, and Z4 map to light, normal, medium, heavy, and extra-heavy interference on the ball-to-raceway contact, and they apply to both caged and full-complement blocks without change [S3][S6]. For a related motion-component decision (back-to-back vs face-to-face angular-contact bearing pairings) that often sits on the same axis as a linear guide carriage, see the angular contact pairing decision map. Preload itself is induced by using balls whose diameter is slightly larger than the distance between the raceways of the bearing block and guide rail, a mechanism that works the same in either retainer configuration [S8].
Two trackable signals for the next 6 to 12 months. First, more profile-rail makers are expected to publish caged variants of their 15-mm and 20-mm HG/HGH-class blocks to compete with NTN's SNR caged line, because the maintenance-interval argument is the strongest commercial lever in factory automation. Second, cage-material options are migrating from standard POM to high-temperature PPA and PEEK grades on the same block geometries, which extends the caged option into higher-ambient applications like automotive paint-line transfer and semiconductor high-temp processing, a segment that today is still mostly full-complement because of the cage temperature ceiling.
For component-level specifications, see crossed roller guide, and ball bearing.