
Ball Screw Straightness Tolerance Across Full Travel
A ball screw’s full-travel straightness tolerance must be stated separately from lead error, mounting flatness and cylindricity, each with its own datum and measurement method.
Read →Industry News · Category
A ball screw’s full-travel straightness tolerance must be stated separately from lead error, mounting flatness and cylindricity, each with its own datum and measurement method.
Read →
Select the ball screw from its equivalent axial load, speed-dependent load factor, basic dynamic rating, and duty-cycle-adjusted L10 life, then verify speed and buckling limits.
Select a vertical-axis ball screw from required axial load, stroke, speed, accuracy and life, then size a spring-engaged brake for worst-case holding torque.
Select a ball screw by diameter, lead, accuracy, preload, critical speed, and axial load, with ground screws for precision CNC axes and rolled screws for general automation.
Choose an end-cap return for high-speed feeds and tight envelopes; choose a return tube for economical fine-lead assemblies where external clearance is available.

Ball screw nut flange bolt patterns are series-specific, with DIN 69051 applying to 16–50 mm flanged metric styles; verify hole counts and dimensions from drawings.
Choose a double-circuit ball nut for preload, stiffness, and sustained accuracy; choose a single nut for compactness, lower cost, and reversible axial load capacity.
Choose horizontal or vertical ball screw bearings by load path: use fixed and floating supports for horizontal shafts, and paired angular contacts for vertical thrust.
A ball screw should not operate at its critical speed. Use the lower of the shaft critical speed, DN-based permissible speed, and nut rating.
Choose oil for sustained high-speed ball screws with heat or precision limits. Choose grease for simpler service unless its retention and contamination risks are controlled.
For 1 µm servo positioning, select the lead from encoder counts per revolution, then verify backlash, repeatability, rigidity, and motor speed.
Ball screw lead error over 300 mm must be read as a bounded travel deviation, not as an error allowed to accumulate along the full stroke.
Hollow shafts enable internal screw cooling, but lose material stiffness; nut cooling can match hollow-shaft capacity without rotary seals.
A ball screw assembly includes the screw, ball nut, and end support bearings, and the two main end-support methods are floating and fixed.
Choose a ball screw for high efficiency, speed, accuracy, and repeatability. Choose an Acme screw for lower cost, higher back-drive resistance, and self-holding behavior.
Lead sets travel per revolution, while the rigidity of the complete screw assembly includes contributions from the screw shaft, ball nut, support bearings, and housings.
Choose a metal bellows coupling for precision ball-screw axes requiring low wind-up; choose a jaw coupling when shock absorption and lower cost outweigh positioning accuracy.
Long-travel ball screw buckling limits depend on root diameter, unsupported length, end fixity, and compressive load. Use Euler limits with at least a 2:1 safety factor.
Specify CNC ball screw backlash from axis demand and baseline: ground screws with preload target 0.000–0.002 in, while rolled C7/C8 assemblies typically run 0.002–0.008 in.
Axial rigidity at maximum load is a system limit, not a single catalog number. Size the screw for load, life, buckling, mounting, and support-bearing stiffness together.
A ball-detent torque-limiting coupling isolates a jammed drive within 3–5 ms, using detachable steel balls and a calibrated spring to disengage at a preset torque.
Ball bearing breakaway torque depends on fit, preload, lubrication, seals, and temperature; specify a maximum startup torque and verify it by test.
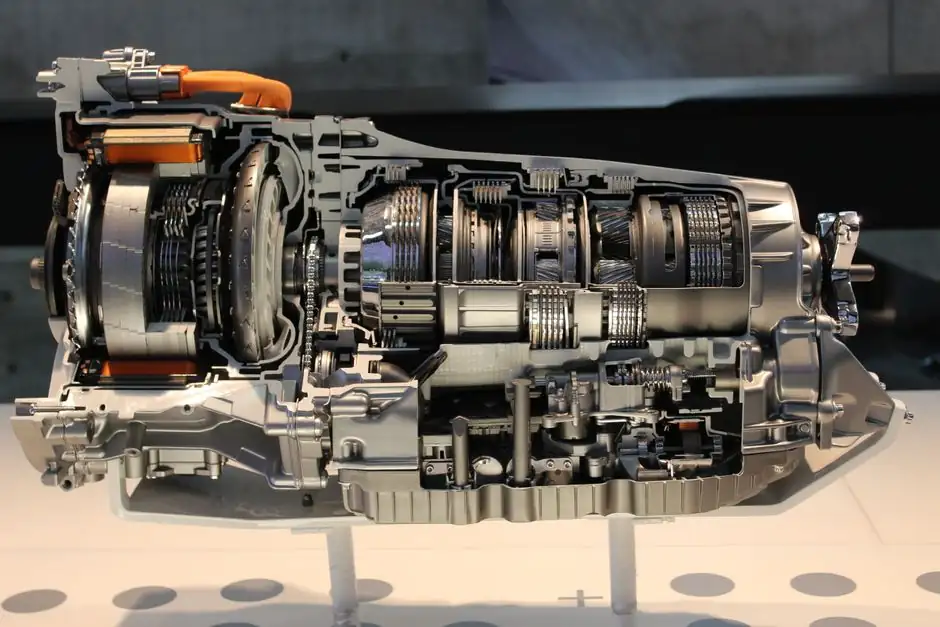
Cold starts fail when grease torque exceeds actuator capability. Specify lubricant, preload, fit, and a measured breakaway margin.
Measure ball bearing radial play unloaded with a standard gage load and dial indicator, then account for fit, temperature, and preload.
Ball bearing raceways typically require 60–65 HRC after tempering, with exact limits set by component design, material, and process.
Grease-lubricated ball bearings typically support 65% to 80% of the limiting speed of oil-lubricated bearings, while oil wins for heat removal and very high speed.
Ball bearing cage pocket clearance and guidance type jointly control cage motion, friction, and stability. Choose the pair from speed, load, temperature, and lubrication data.
Ball bearings are specified by bore, outside diameter and width, not bore alone. For a 3–200 mm bore range, select the series and configuration against verified dimensions.
ATEX-certified jaw couplings suit Zone 1 pump drives when the unit has documented explosive-atmosphere conformity and derated torque, speed, and misalignment limits.

An anti-flail spacer retains coupling parts after membrane failure, limiting ejection risk while requiring a design independent of coupling bolts and guards.
An arc of contact below 180° reduces V-belt power capacity; correction factors range from 0.99 at 174° to 0.65 at 83°.
Choose apron pan conveyor chain for heavy, hot, abrasive, or fine bulk material on inclines; use standard attachments for lighter, cleaner, faster handling.
Choose a rack-and-pinion anti-creep cage when vertical, shock-loaded, reversing, or partial-stroke operation risks cage drift; use a standard cage where loads and travel are benign.
An anti-backlash nut reduces lead-screw reversal error, but a standard nut is often adequate for moderate loads. Compare preload, load, wear, cost, and accuracy.
ANSI and ISO metric roller chains are not interchangeable: match pitch, roller, pin, plate, width, strength, and sprocket specifications.
Tapered roller bearings can provide greater spindle stiffness than angular contact ball bearings, but their lower speed capability and installation complexity require careful evaluation.
Angular contact bearings suit higher unidirectional axial loads; deep groove ball bearings suit lower axial loads with bidirectional thrust and lower cost.
Spindle designers should specify a matched angular contact bearing set by contact angle, preload, arrangement, speed rating, and measured runout.
An angular contact bearing has no universal breakaway torque. Specify from preload, contact angle, lubrication, load and temperature, then verify the assembled unit.
Phenolic cages suit high-speed angular contact bearings when low inertia and heat control dominate; steel cages suit higher-temperature, shock-prone service.
Fine-tune angular contact bearing preload with precision shims, measured axial displacement, and controlled assembly torque, avoiding excessive friction, heat, and premature bearing damage.
Specify spindle runout by measurement, arrangement, and load path, not ABEC class alone; ABEC 7 bearings can show materially different assembled-axis error.
Machined brass cages suit heavy loads, shock, and severe service, while ribbon cages are among the available cage options for angular contact ball bearings.
Specify angular contact bearing raceways at 58–62 HRC for typical steel configurations, then verify the delivered hardness and component-to-race difference.

Angular contact bearing preload classes A, B, and C set light, medium, and heavy preload, trading lower heat for higher stiffness and load capacity.

P4 angular contact bearings use ABEC 7 or equivalent dimensional accuracy for machine-tool spindles requiring high rigidity, accurate guidance and high speed.

Grease-lubricated angular contact bearings are commonly limited to 65% to 80% of the limiting speed available with oil lubrication. Oil-air systems suit higher speeds.
For inverter-driven motor shafts, compare ceramic-coated and silicon-nitride hybrid bearings by dielectric voltage, load capacity, speed, and high-frequency discharge protection.

Flush-ground angular contact bearings permit controlled duplex preload, while standard-face sets may require spacers or matched clearance. Choose DB, DF, or DT by load direction and moment duty.

A 25° angular contact bearing has no universal dynamic load rating: rating depends on bore, geometry, and series. A 7206 ACBB example combines 17.8 kN radial capacity with about 8.5 kN axial capacity.

Angular contact bearing preload is not self-retaining: position preload can relax as the assembly runs in, so cartridge retention depends on fit, spacing, and controlled axial clamping.
For high dₙ operation, select the cage from speed, temperature, load and lubricant data, not from material name alone. Brass, engineering polymer or steel cages suit different envelopes.

Angular contact spindle bearings commonly cover 6–120 mm bores, with 6–25 mm typical for compact precision units and 120 mm as an upper series limit.
Angular contact ball bearings suit combined radial and axial loads, while angular contact thrust bearings prioritize axial stiffness and thrust capacity.
Aluminum crossed roller guide rails cut stage mass by roughly two-thirds versus steel, but steel wins where impact, stiffness, and extreme load dominate.

Choose an aluminum worm reducer for lower mass, easier installation, and corrosion resistance; choose cast iron for shock loads, high torque, and vibration damping.

Add cylinder force work to impact kinetic energy, then check per-cycle capacity, hourly heat load, force, and stroke limits.
Choose ACME for 29-degree imperial systems and Tr for 30-degree metric systems; match pitch, lead, handedness, and load before ordering.
PEEK lead screw nuts suit higher-temperature service than acetal, but load, lubrication, chemical exposure and duty cycle decide the safe material choice.
Acetal shaft collars suit light, corrosion-sensitive assemblies, but metal collars provide substantially higher axial holding power and should handle demanding loads.
For light-load, quiet mechanisms, acetal is the default plastic gear choice; nylon suits tougher, moisture-exposed parts, while steel remains preferable for high torque and heat.
Accumulated pitch error tolerance limits how far a timing pulley can depart from ideal tooth spacing. Specify pitch, profile, tooth count, and pulley size before setting the allowable error.
ABEC 7 and ISO P4 map to nearly equivalent high-precision bearing classes. Verify size-specific tolerances, runout, clearance, and load data before substituting one label for the other.
For a 20 mm bore, ABEC 1, 5, and 7 reduce dimensional variation progressively; ABEC 7 is for high-precision shafts, not ordinary machinery.
440C stainless steel ball screws suit cleanroom and vacuum stages when the design controls lubrication, outgassing, preload, and particulate release.
Choose quenched-and-tempered 42CrMo4 for high-strength, fatigue-critical rings; use 50Mn only where its lower-cost, non-alloy design meets the load case.
A 40° ribbed-pulley groove suits many serpentine and multi-rib drives, but groove angle alone does not define fit; rib pitch, tip radius, and sheave size must match the belt.
A 31313 tapered roller bearing with a 65 mm bore, 140 mm outside diameter and 36 mm width handles heavy combined radial and axial loads.
For a 25 mm bore, 30205, 32205, and 33205 share a 52 mm outer diameter, but their widths and load capacities increase progressively.
Choose 15° bearings for high-speed, light-thrust spindles, 25° for balanced combined loads, and 40° for maximum axial capacity at lower speed.
Choose 14.5° for replacement compatibility and 20° for higher root strength, then verify tooth form, undercut risk, and shaft loading.
For a 45 mm shaft, specify a 14 × 9 mm parallel key with a 5.5 mm shaft keyseat and a 3.8 mm hub keyway.
Select spring washers by joint load, vibration, temperature, corrosion exposure, and required travel, then verify each production lot for geometry, heat treatment, and surface condition.
Select Belleville spring washers for pulp and paper joints with high load, vibration, and thermal movement, matched by diameter, material, and load-deflection data.
Belleville disc springs best suit high-load agricultural joints, while wave washers control lighter vibration and shock. Match washer size, load, stack, material, and deflection to the service.
Marine spring washers should match bolt size, joint load, movement, and saltwater exposure. A 316 stainless M36 DIN 127B washer has a 56 mm outside diameter.
Wind turbine spring washers must match joint load, movement, corrosion exposure, and installation method; Belleville discs suit high-load drivetrains, while split washers suit anti-loosening joints.
Select Belleville disc washers for high-load packaging joints, wave washers for lighter vibration control, and split lock washers for low-cost anti-backoff duty.
Select stainless-steel wave or Belleville washers for food-processing joints, prioritizing cleanability, corrosion resistance, load, and corrosion behavior.
Belleville disc springs specified in 17-4 PH stainless or Inconel 718 are the default for steel mill bolted joints above 480°F, with DIN 2093 Series C stacks delivering up to 100 kN per 63 mm disc. Lock washers and wave washers cover sub-250°F auxiliary duties only.
Automotive production lines typically specify Taper Lock bushes in the 1008 to 3535 series with metric bores from 10 mm to 90 mm, C45 carbon steel or GG25 ductile iron bodies, and 1:12 taper clamping for 0.2 to 90 N·m screw torque. Selection is driven by shaft RPM, ambient coolant and oil exposure,
Taper bush selection for pulp and paper drives reduces to three decisions: bush family (Taper Lock vs QD vs split-taper), metric bore per BS 4235 Part 1:1972, and material grade suited to wet, corrosive, high-temperature mill zones. Match the hub to the existing bushing series, then size the bore to
Marine-duty taper bush selection hinges on a 1:12 (8° included) taper to BS 4235 Part 2, with 316L/stainless options for salt-spray service. Match series 1008-5050 to hub bore, then derate torque by 15-20% for saltwater deck machinery.
For packaging line shafts running 50-500 RPM in washdown zones, 302/304 stainless spiral retaining rings with carbon-steel options for dry sections, matched to shaft DIN 471 or ANSI metric standards, give the cleanest service life.
For wind power drivetrains, taper bush selection hinges on series/bore matching, material grade, and wedge torque margin, not on bush family. Specify 3535/4545 series or larger, ISO-keyed bores per BS/UNC, GG25 or ductile iron as a baseline, and verify cap-screw torque against hub draw-screw count b
For marine shaft work, specify 316 stainless steel two-piece clamp collars with 1.125" OD and 0.406" thickness as the baseline; avoid set-screw and carbon-steel collars in saltwater service due to crevice pitting and galvanic loss.
For food processing lines, specify 302 or 316 stainless steel retaining rings in a passivated finish, with a machined groove and a multiple-turn or reinforced design for cleanability and corrosion resistance. Carbon steel rings fail washdown; 316 SS adds chloride resistance.
For material handling conveyors, a two-piece clamp-type stainless or zinc-plated steel shaft collar rated heavy-duty is the default choice, with bore sized to shaft tolerance and face-to-bore perpendicularity verified for load-bearing stops.
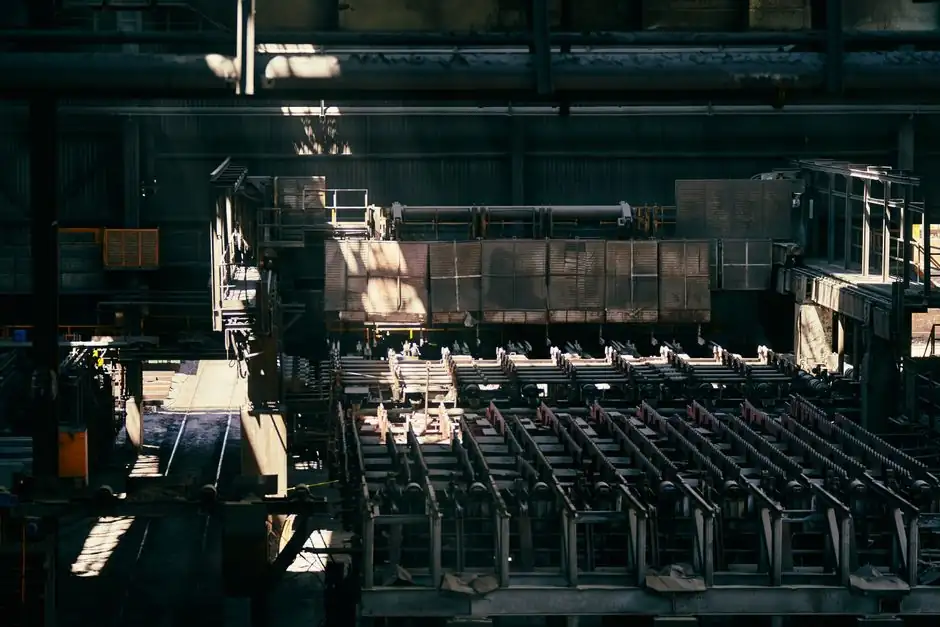
Steel mills need retaining rings that survive heat, scale, water, and cyclic impact; spec carbon spring steel (SAE 1060-1090) for cost-driven picklers and conveyor rolls, 302 or 316 stainless for hot, wet, or acid zones, and choose Spirolox/spiral or reinforced constant-section rings over standard s
Taper Lock bushes with a nominal 8° taper (1 11/16" per foot, ≈14.06%) are the dominant shaft fixing for material handling conveyors, with stocked sizes from 1008 (≈9 mm bore) up to 120100 (≈254 mm bore) per MPTA-B9i-2013. Selection is driven by shaft bore, transmitted torque, hub type (weld-on, bol
Shaft collar selection for packaging lines hinges on matching holding mechanism (set-screw vs single-split vs double-split clamp) to hygiene, changeover frequency, and shaft material, with 303/316 stainless or anodized aluminum as the dominant wet/washdown choices. Quick-clamping designs el
For food processing shafts, specify 303 or 316 stainless steel, FDA/USDA-compliant shaft collars in one-piece clamp or two-piece split styles, with bore sizes from 1/4 in. to 10 in. (6 mm to 250 mm), and verify optical detectability for metal-detector lines.
For cement plant applications, retaining ring selection is driven by abrasive dust, temperatures to 200°C, heavy vibration, and high thrust loads on crusher, kiln, and conveyor shafts. The practical starting point: specify stainless or coated rings in housings above 3 in. diameter, favour spiral or
Parallel square or rectangular keys per ANSI B17.1 are the default shaft key choice for textile-mill drives up to about 20 in. shaft diameter, sized on torque, shaft diameter, and bearing/shear stress limits. Woodruff, taper, and feather keys cover special textile cases like sliding hubs or light-du
Heavy-duty and ultra heavy-duty shaft collars in 316 stainless or zinc-plated steel with set-screw or two-piece clamp construction are the standard spec for mining service, sized for shock load, abrasive contamination, and corrosion. Selection hinges on holding power, face-to-bore perpendicularity,
For mining-duty retaining rings, specify external reinforced or heavy-duty axial styles in corrosion-resistant alloys, with groove geometry validated for shock and vibration loads above standard industrial duty.
Shaft keys for automotive production lines are typically parallel or splined, selected by torque, shaft diameter, hub length, and material match to BS 4235, ASME B17.1, or DIN 6892. Standard square and rectangular parallel keys suit gearbox and pulley hubs, while involute splines dominate high-torqu
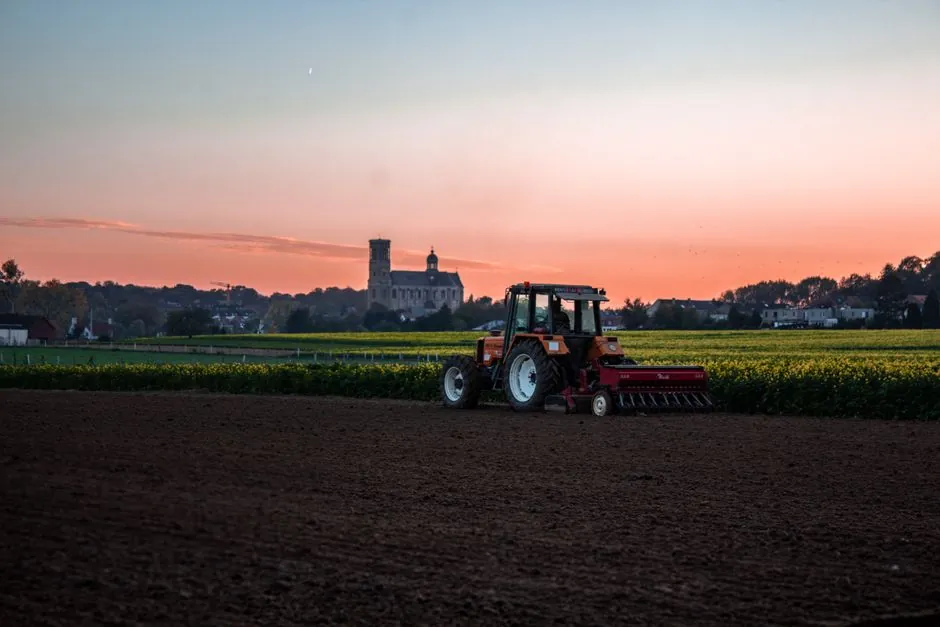
Shaft key selection for agriculture machinery hinges on shaft diameter, torque load, and the level of axial movement allowed between the hub and the shaft. Parallel square and rectangular keys dominate the segment, while Woodruff keys serve light-duty tapered shafts and taper keys handle reversible,
Marine propeller shaft keys are usually rectangular parallel keys sized to shaft diameter, with 316 stainless or silicon bronze chosen for corrosion resistance over carbon steel. Sizing follows BS 4235 / ASME B17.1 / DIN 6892, with material grade, immersion duty, and dismantling access driving the f
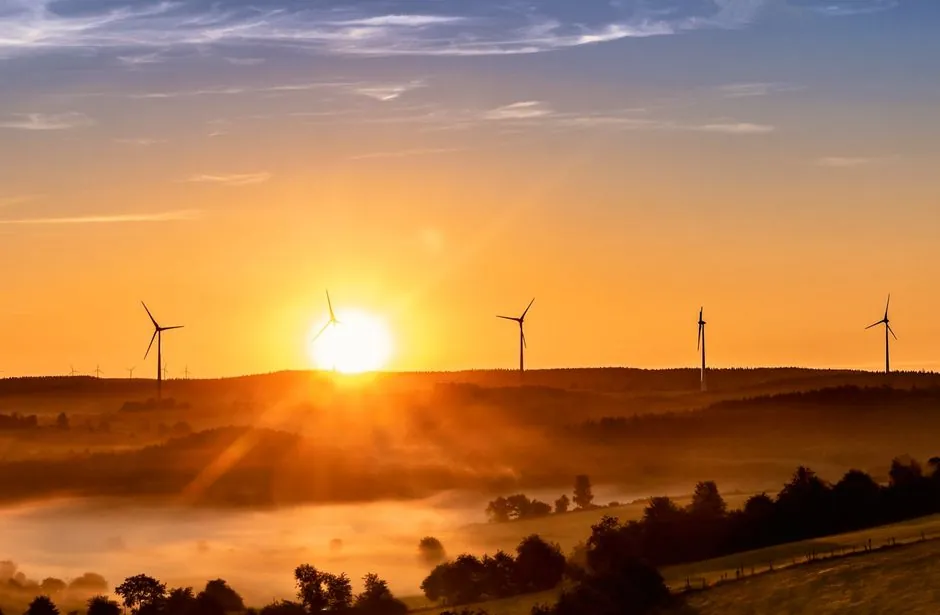
Parallel rectangular keys remain the default shaft key choice for utility-scale wind turbine drivetrains, sized to shaft diameter (1–20 in.) and rated for unidirectional torque with periodic hub withdrawal. Woodruff keys suit small shafts (0.25–2.5 in.) but lack the torque capacity for main-shaft or
Taper locking assemblies let textile mills mount pulleys, gears and rollers on shafts without keyways, with self-centering concentricity as tight as 0.04 mm and zero-axial-displacement options for precision drives. Selection for textile drives comes down to shaft diameter, hub bore, transmissible to
Taper bush selection for food processing is governed by three non-negotiables: stainless or food-grade coated construction, IP66+ washdown sealing of the hub, and a shaft lock method sized below 5 in. Taper Lock ceiling. Spec the bushing series and material first, then match the hub and hygiene enve
Marine belt tensioner selection pivots on engine model, belt type, and corrosion exposure: Gates catalogs 500+ tensioners globally, Ilmor MV8V-1134 fits Ilmor marine engines, and ElectroMaax supplies Yanmar and Nanni-specific units at $249–$279.
Pick an automatic spring or elastomeric belt tensioner sized 32-396 N for packaging lines below 6 m/s, matching roller width to belt width and material to washdown or dry-food environments. Manual screw tensioners suit only low-duty, accessible drives.
Retaining ring selection for wind turbines centers on matching ring type, material yield strength, and groove geometry to rotor, gearbox, and pitch/yaw loads. Smalley stocks a dedicated Wind Power Series up to 120 in diameter, while generator retaining rings typically need 175-200 ksi yield strength
V-ribbed belts for food processing are typically polyurethane V-ribbed constructions in PJ, PK, or PL profiles, paired with stainless or food-grade coated pulleys and HACCP-compliant tensioners, and selected against the same four rules as any food-contact belt: FDA 21 CFR food-contact compliance, wa
Retaining ring selection for material handling hinges on five decision gates: assembly type (shaft vs housing), groove geometry, thrust load class, installation method, and environment. Matching carbon spring steel, stainless, or specialty alloys to the duty cycle and corrosion profile prevents the
V-ribbed belts suit mining auxiliary drives with compact pulleys, high RPM, and tight alignment, but are not the right pick for the main conveyor or crusher power take-off where classical V-belts dominate.
Silent chain selection for packaging lines hinges on synchronizing high-speed drive trains, matching tooth count to sprocket ratio, and selecting stainless or coated materials for washdown environments. Specify SC or 06B/08B silent chain class when noise below 75 dB(A) and speeds above 1,000 rpm are
Silent chain drives in cement plants handle high-shock, dust-laden, high-temperature service where inverted-tooth geometry gives quieter, smoother engagement than roller chain. Selection centers on pitch, tooth flank angle, horsepower, ambient temperature, and dust ingress, matched against the alter
Silent chain suits mining drives where high speed, low noise, and accurate timing matter, but is not a drop-in replacement for heavy-series roller chain. Use ANSI B29.2M-1982 sizing, harden tooth profile and pin material, and size sprockets for the dust and shock load profile of the service.
V-belt selection for wind power pitch and yaw drives hinges on matching ISO/RMA cross-section (SPA, SPB, SPC) to design kW, applying a service factor of 1.3–1.8 for variable-torque loads, and verifying a 95% peak efficiency window with retensioning every 3–6 months per DOE guidance.
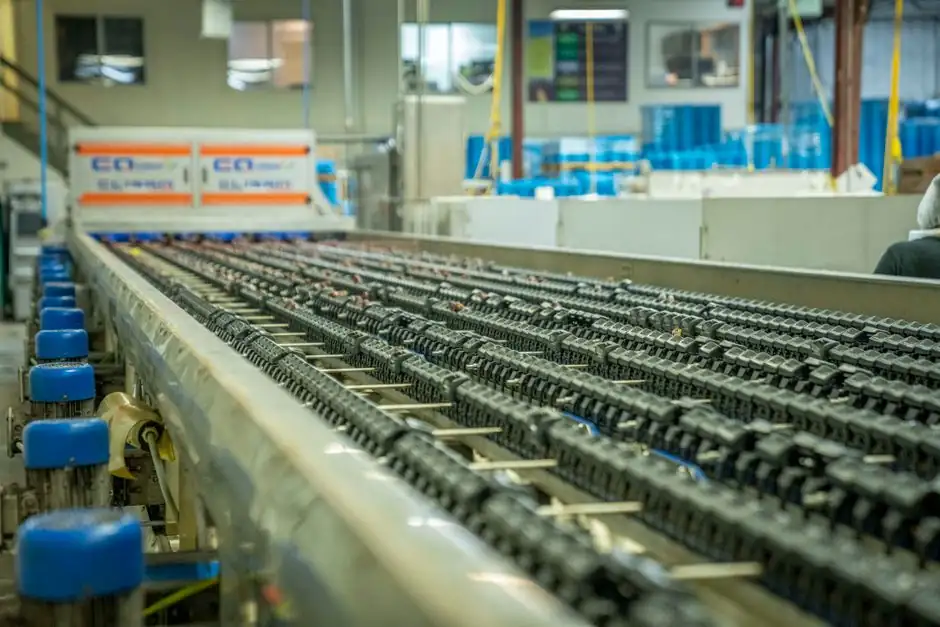
Pulp and paper mills run conveyor chains in wet, acidic, abrasive conditions that drive a single dominant failure mode: corrosion-driven wear on wood-yard drag lines, pulp prep, and paper-roll handling. Select chain family by zone, harden pins and bushes, and specify automatic lubrication to keep se
Classical A/B/C/D/E and narrow wedge SPZ/SPA/SPB/SPC V-belts cover the bulk of material-handling drives; selection hinges on design horsepower (actual HP × service factor 1.0–1.8), pulley diameter, and compound choice (EPDM for heat, neoprene for oil). Cogged or narrow-wedge profiles win on small-pu
V-belt selection for packaging lines hinges on matching the classic A/B/C/D/E or narrow SPZ/SPA/SPB/SPC cross-section to design horsepower, service factor (typically 1.0–1.8), and pulley geometry, then verifying pitch length, wrap angle, and tension on the specific conveyor, flow-wrapper, or cartoni
For food processing V-belt drives, specify wrapped or polyurethane V-belts with FDA- and EU food-contact compliance, use a service factor of 1.2-1.6, and size by design horsepower, shaft RPM, and pulley minimums to avoid premature failure and contamination risk.
V-belt selection for cement plants is driven by service factor, dust load, and ambient heat: classical A/B/C/D sections and narrow-wedge SPZ/SPA/SPB/SPC covers most conveyor, crusher, and mill drives, with EPDM or aramid-cord construction preferred for 60-90 degree C kiln-zone environments.
For textile mills, timing belt selection is dictated by machine type, profile family (T5/T10/AT5/AT10, 5M/8M, GT2, XL/L/H), and ambient stress: stenter frames demand heat resistance at 150-220°C, rapier and air-jet looms need 600-1200 RPM synchronization, and dyeing machines require chemical/moistur
Mining duty cycles, contamination, and shock loads make HTD or GT2 curvilinear timing belts the default for drives up to roughly 50 kW, while trapezoidal XL/L/H series remain in service on legacy mills. Selection is governed by Design Power (Pd = Pt × Ks) with Ks composed of load, idler, speed-ratio
For 2026 automotive production, specify roller chain sprockets to ISO 606 / ASME B29.100, choose steel for high-stress drives, stainless for corrosion zones, plastics only for low-load timing, and hold a minimum of 17 teeth on high-speed shafts to control wear.
Roller chain selection for textile mills is driven by pitch, service factor, and material grade: small-pitch precision chain for high-speed light loads, multi-strand chain for heavy shock loads, and stainless or nickel-plated chain for humid, dye-laden, or chemical finishing environments per OEM gui
Pulp and paper mill sprocket selection hinges on three decisions: tooth count (17+ on drives), material (cast iron, flame-hardened plate steel, stainless), and matching chain pitch to a calculated design horsepower with the correct service factor. Material choice is dictated by corrosion, abrasion a
Roller chain selection for automotive production lines follows a 9-step engineering flow: classify driven load, apply a service factor (1.0-1.7), compute design HP, pick pitch, and pair with sprockets holding a minimum 120° wrap angle. Spec chains to ANSI B29.1 or ISO 606, use stainless or nickel-pl
Specifying a timing belt for an automotive production line comes down to four decisions: ISO 9010/9011 ZA or ZB profile for engine-class service, curvilinear HTD or GT2/GT3 teeth for high-torque transfer, chloroprene rubber with steel or glass tension cord for the -20 to +80 C window, and a matched
Selecting a sprocket for agriculture machinery comes down to matching ANSI/ISO chain size, tooth count ratio, hub type, and induction-hardened mid- to high-carbon steel to the dust, shock, and corrosion load of the application.
Roller chain selection for pulp and paper mills combines standard ANSI drive-chain sizing with mill-specific chain constructions: steel bushed roller, welded steel mill, gull wing roll, and heat-treated G70 transport chains. Source data was published on 2026-10-11.
Roller chain selection for agriculture machinery hinges on matching ANSI chain size (#40-#100), strand count, and duty class to the driven load, speed, and shock profile. Premium ASME/ANSI chains suit combines and balers; steel detachable links stay under 400 ft/min in dirty, low-speed work.
Marine propulsion and deck drives commonly specify ANSI B29.1 roller chain in 40-1 through 80-1 pitch, marine-grade stainless (typically 304 or 316) or nickel-plated carbon steel, with service factors of 1.4-1.7 per ISO/Renold guidance for moderate to heavy shock loads from wave slamming.
Roller chain selection for wind turbine pitch and yaw drives follows the standard service-factor method, with multi-strand ANSI chains (40B-120B) commonly used where torque and shock loads exceed single-strand capacity.
Spec a timing belt for pulp and paper mills by matching tooth profile (HTD/RPP/T10) and pitch to drive load, then verify with at least six teeth in mesh, flange rules per center-distance ratio, and surface speed below 28 m/s for large-pitch and 50 m/s for minipitch belts.
Roller chain for material handling is selected in five steps: classify the driven load, apply a service factor (1.0 uniform to 1.7 heavy shock), compute design HP, pick pitch from an HP/rpm quick selector, then size the small sprocket teeth count using ISO 606 ratings.
ANSI #40-#80 roller chains dominate packaging-line drive and conveyor duty; pick chain pitch from design HP, service factor, and small-sprocket RPM, then match material to wash-down, heat, or dust exposure. Stainless 304/316 is required only for hygienic or corrosive zones, not the whole line.
Cement plants run roller chain above 1.5" pitch in dust, heat, and shock-loaded service on kilns, bucket elevators, and apron conveyors. Selection is governed by ISO 606 dimensional chains, design horsepower = HP × service factor (Ks 1.0–1.7), and heavy/attachment variants such as cement-engineered
Timing belt selection for agricultural machinery follows the same five-variable logic as industrial drives: trapezoidal XL/L/H or metric T2.5/T5/T10 profiles suit light-duty implements, while curvilinear HTD 8M/14M or GT2/GT3 profiles handle high-torque combine and baler loads, with neoprene chlorop
Mining-duty roller chain selection starts with five fixed inputs (HP, RPM, shaft diameters, center distance, drive class) per ANSI B29.1 / Renold selection flow, then layers a service factor of 1.0–1.7 to set the design HP. For heavy-shock, abrasive, or corrosive mining service, heavy series or mult
Marine timing belt selection starts with profile and pitch (HTD 5M/8M or GT2 for saltwater service), then enforces 90° minimum wrap, corrosion-resistant pulleys, and derated service factor. With proper cover material and tensioning, service life reaches 15,000–30,000 hours.
Hydraulic shock absorbers in textile mills must be sized by impact velocity and per-cycle energy, not average velocity. For cyclic rates above 240/hour, apply a 30% safety factor on energy capacity. Use self-compensating (adjustable) units where mass or speed varies more than 25%; use fixed-ori
For automotive production lines, shock absorber selection is driven by OE damping specification, vehicle class, and the type of construction required. Twin-tube hydraulic dampers dominate passenger cars, with piston-rod, valve-group, and bushing quality controlling fatigue life.
Industrial shock absorbers for pulp and paper lines are sized on input energy per cycle in Nm, effective mass in kg, propelling velocity in m/s, and cycles per hour, with hydraulic adjustable units dominating roll and conveyor stops. ACE MAGNUM MA6450 (2,275 Nm/cycle, 220–50,000 kg) and Enidine OEMX
Timing belt selection for utility-scale wind turbines centres on HTD or GT2/GT3 curvilinear profiles in 8M and 14M pitch, sized by design power (motor kW × overload coefficient) and validated against tooth shear strength, not just rated power. Yaw, pitch, and auxiliary drive duty cycles differ enoug
Sprocket selection for material handling comes down to matching ANSI/ISO chain pitch, tooth count, hub style (A/B/C/D), and material to load, speed, and corrosion duty. Steel and hardened alloy dominate heavy conveyor service; stainless and engineering plastics cover washdown and lightweight lines.
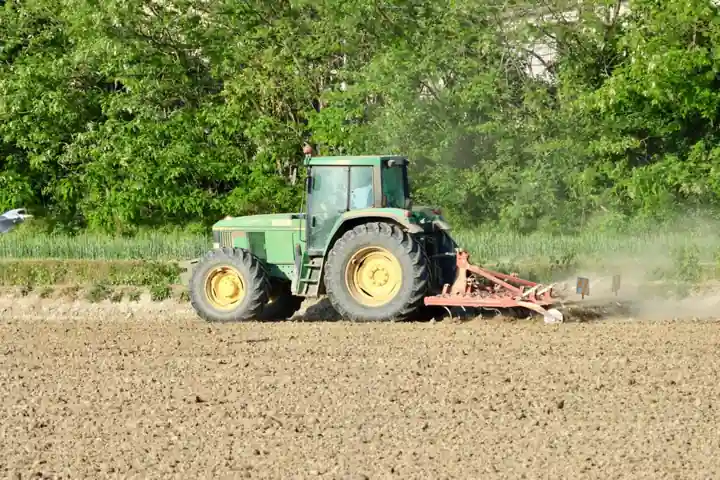
Agricultural shock absorbers should be sized for impact velocity (not average velocity) using kinetic energy plus drive work, with a 10–20% stroke margin and a >150% peak-load safety factor, then derated for cycle rate to avoid seal failure.
Timing belt selection for material handling hinges on four gates: pitch and profile (HTD/GT2 vs trapezoidal), tensile cord (fiberglass/polyester/Kevlar), elastomer (neoprene vs polyurethane), and tooth/pulley fit. Match these against load, surface speed (≤50 m/s for minipitch), FDA/washdown needs, a
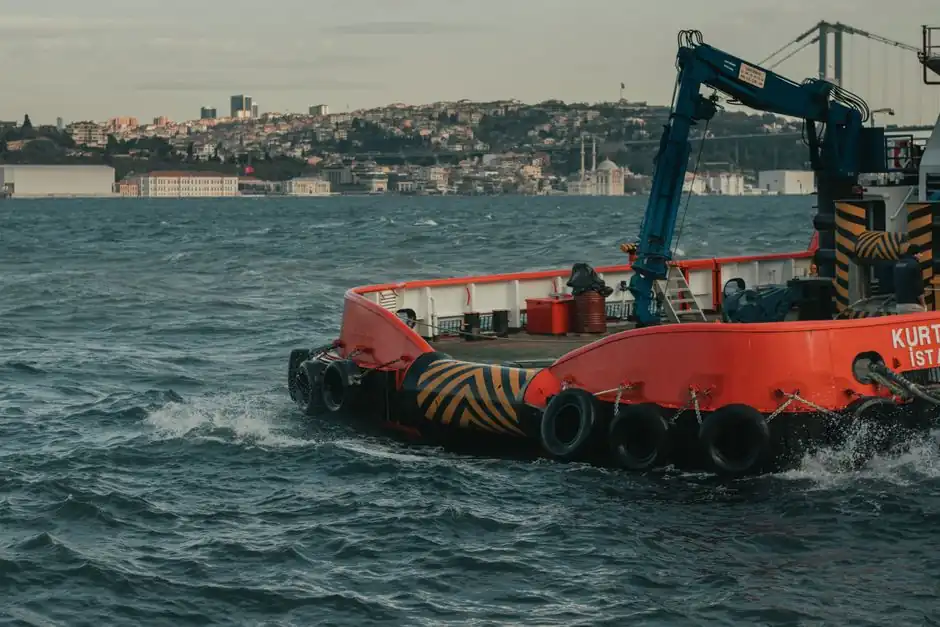
Marine shock absorber selection splits into three families: polymer mooring snubbers (1,000-15,000 kg break load, recreational docks); engineered rubber and elastomer fenders (0.5-2.0 m/s impact, 5,000+ tonne supply vessels per NORSOK N-003); and rubber machinery mounts (0.45-2,200 kg per mount) for
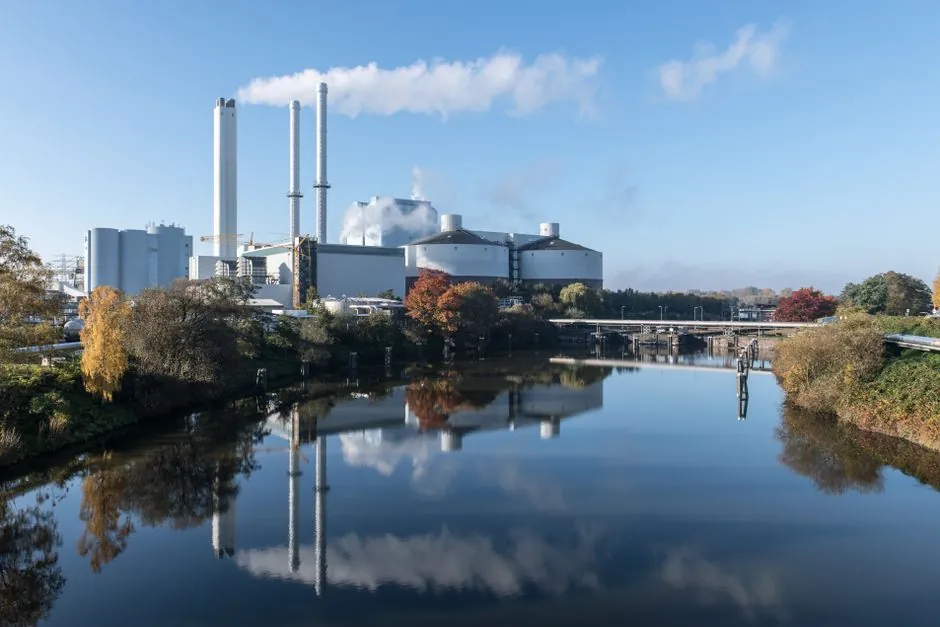
Fluid couplings in pulp and paper mills are most often specified on refiners, stock and water pumps, ID/FD fans, and chipper conveyors, where they provide no-load motor start, soft acceleration, overload slip, and variable-speed scoop control. Selection turns on driven-machine inertia (WK²), peak lo
Fluid couplings sized for agriculture machinery should be selected on motor kW, peak load inertia, and duty cycle, with constant-fill units for steady loads and variable-fill units for soft-start protection of conveyors and PTO-driven implements.
For wind turbines up to 12 MW, hydrodynamic fluid couplings (e.g. Flender FLUDEX) sit between the high-speed gear stage and the generator, delivering a soft start, torque limitation, and torsional damping without mechanical contact between the pump and turbine wheels. Selection hinges on motor power
Fluid couplings for material handling are selected by matching constant-fill versus fill-controlled designs to load type, total system inertia, and startup torque, with mineral-oil HLP fluid at ISO VG 32 as the standard working medium. Wrong selection typically shows up as overheating, gearbox wear,
Select conveyor chain for agriculture machinery by matching pitch series (A vs C double-pitch, CA550/CA557, pintle 667X/88K) to the implement's shock load, debris exposure, and ANSI/ASME B29 compliance for wear life.
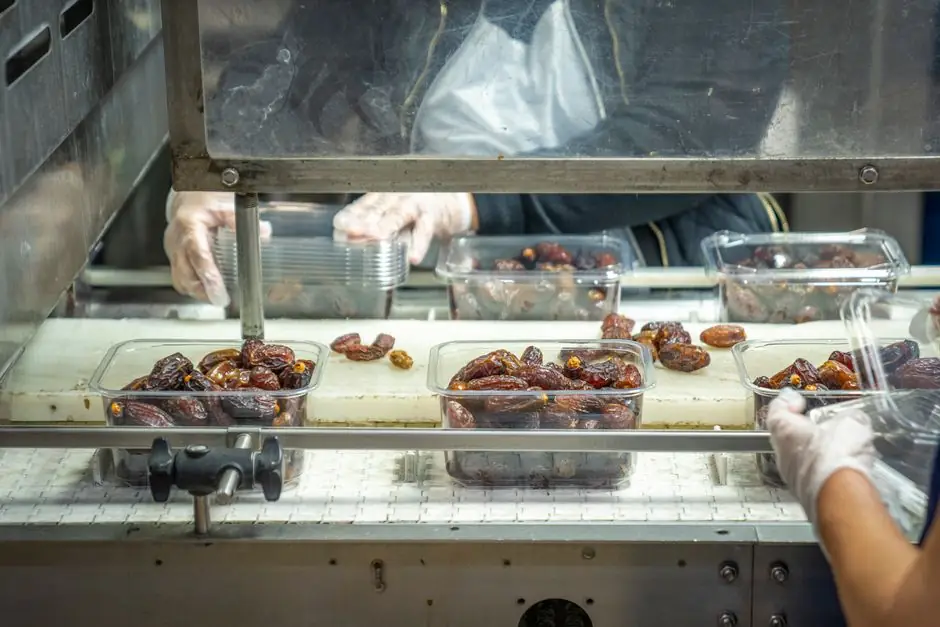
Food-grade timing belts for processing lines must be FDA 21 CFR-compliant polyurethane with encapsulated tension members, selected by tooth profile (5M, 8M, XL, T5), cord type (steel, fiberglass, Kevlar), and operating temperature down to -40°F.
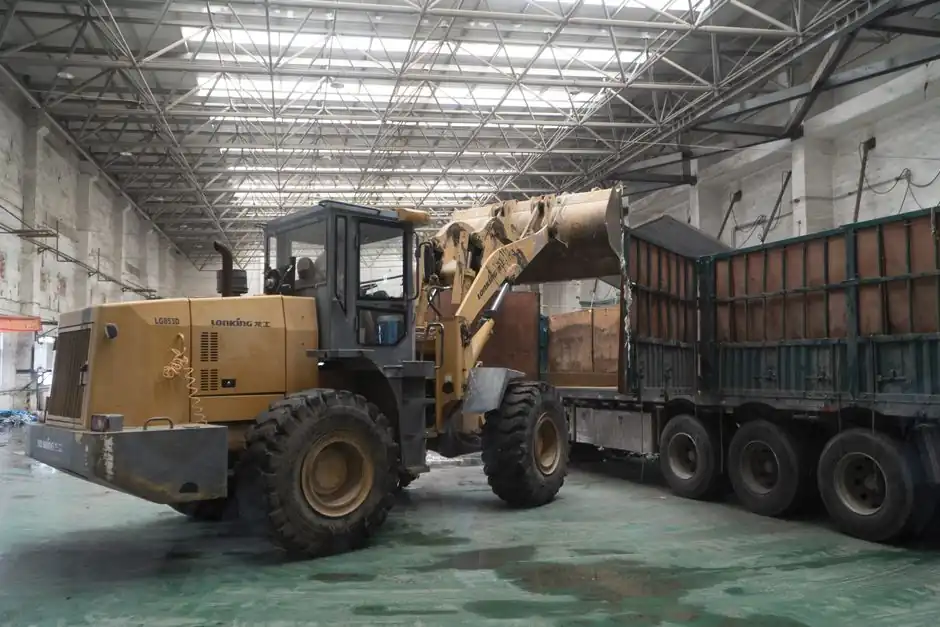
Industrial shock absorbers for material handling are sized on four datasets, effective mass, impact velocity, propelling force, and cycle rate, with 85% efficiency as a baseline and a 30% safety factor above 240 cycles/hour. Fixed units suit predetermined loads, adjustable or self-compensating units
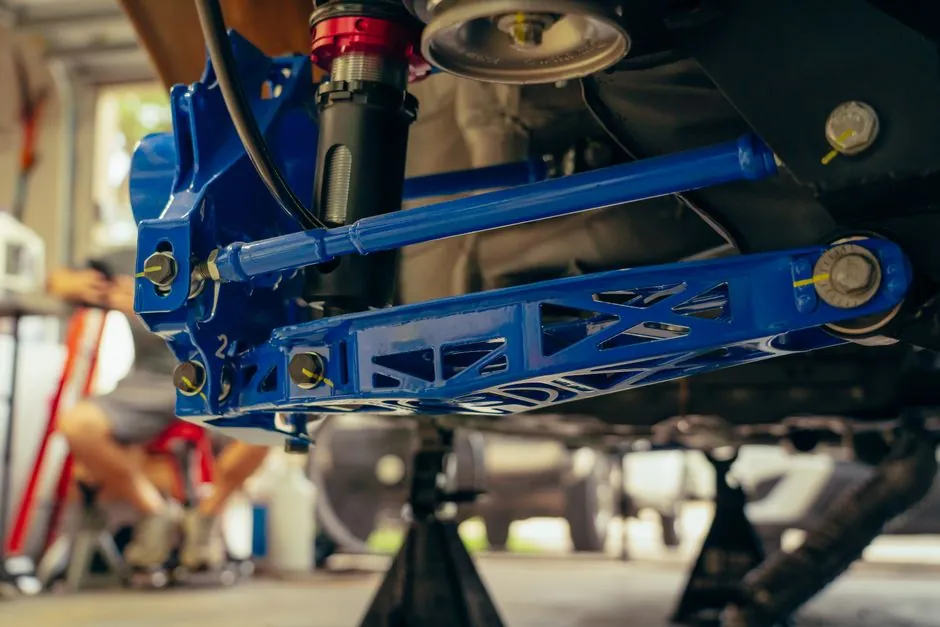
Industrial hydraulic shock absorbers on packaging lines must be sized to impact velocity, not average velocity, with a 30 percent safety margin on energy capacity above 240 cycles per hour. Fixed, self-compensating, and adjustable models each map to specific load, speed, and duty-cycle envelopes.
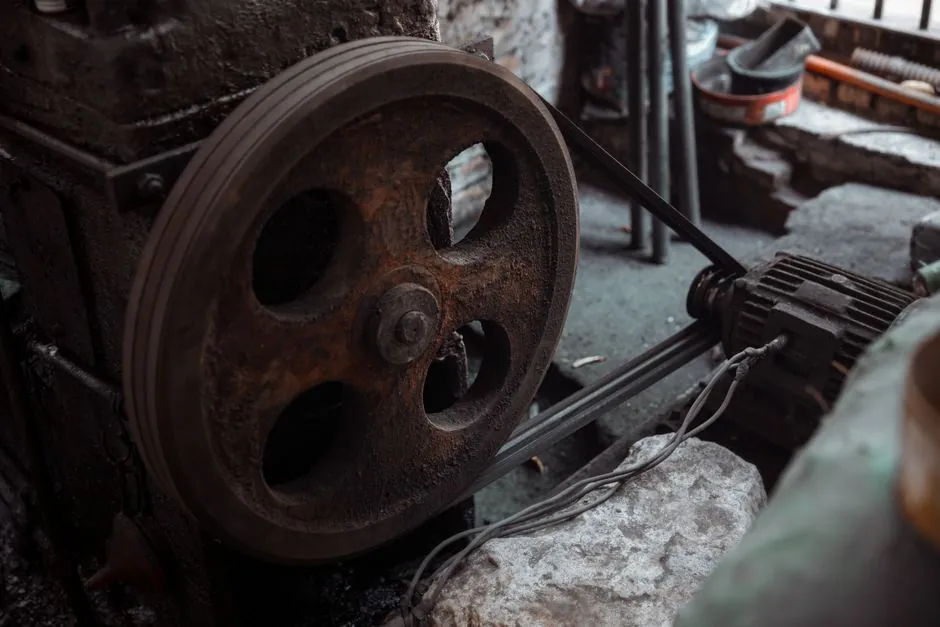
Steel-mill timing belt selection is driven by pitch family (HTD, GT, XL), tensile cord material (steel vs fiberglass vs aramid/Kevlar), tooth profile, and ambient temperature around 80-120°C near continuous casters and rolling mill coiler drives.
Food-grade shock absorber selection hinges on stainless steel construction for washdown resistance, with sizing driven by effective mass, impact velocity, propelling force, and cycle rate. ACE, Festo, SMC, and Taylor Devices publish the core sizing inputs used in 2026 food-line retrofits.
Industrial shock absorbers for cement plants are typically hydraulic self-compensating units sized by absorbed energy E = E1 + E2, with SMC RB series covering 0.3–50 kg impacting mass and 0.1–1 m/s collision speeds. Selection criteria pivot on impact mass, collision velocity, cycle rate, stroke leng
Fluid couplings in steel mills are sized for shock-load absorption on hot-strip coilers, roller tables, and sinter conveyors, with torque capacities up to 66,000 in-lb and starting torque adjustable from 120% to 250% of full load. Specify a constant-fill or variable-fill hydrodynamic unit between mo
Fluid couplings (hydrodynamic couplings) are the standard soft-start and overload-protection device on cement plant conveyor, crusher, kiln, and mill drives, where motors from 300 W to 6 MW can be matched. Selection turns on four decisions: drive train layout, load profile (constant/variable/shock),
For automotive production lines, select universal joints by torque class, series size, material, lubrication strategy, and supplier QA. Steel forged u-joints in 1000-series to 1810-series cover most light to heavy-duty assemblies.
Shock absorber selection for mining hinges on matching energy-per-cycle (J) and cyclic rate to the specific shock profile of the host machine, with a 30% safety factor above 240 cycles/hr per OEM guidance. Hydraulic accumulators address pressure spikes, elastomeric TecsPak bumpers handle high-l
For radial spherical plain bearings per ISO 12240-1, Group 3 (C3) is the loose class with clearance greater than Group N (CN/normal), and is specified where press fits or large inner-to-outer ring temperature differentials would otherwise drive running clearance toward zero. C2 is the tight class be
Fluid couplings for automotive production lines are selected by matching power (kW/HP), speed (RPM), load profile, and slip tolerance, with constant-fill units suited to steady loads and fill-controlled units to high-inertia or shock-loaded drives such as conveyors, presses, and paint-shop transfers
ZA, ZI, ZK, and ZN are four cylindrical worm thread profiles, each defined by which section of the worm the straight tooth flank is drawn in, axial, normal, or radial. Choosing among them is a manufacturing-driven decision: ZA is the easiest to turn and hob, while ZK and ZN require form-ground or ho
Single-stage worm gear reducers commonly span 5:1 to 100:1 ratios; below 20:1, run-in efficiencies reach 90% or higher, but efficiency falls as ratio rises, making higher ratios best for low-speed, high-torque, self-locking duties like conveyors, hoists, and mixers.
At 1450 rpm input, a single-stage worm gear reducer with a 30:1 ratio delivers roughly 48.3 rpm output and output torque scaled by ratio times efficiency. Catalog models such as the Dalton 303 series show 3.15 hp at 1450 rpm with 4032 lb-in torque at 18.75 rpm on the 16:1 double-reduction unit.
Zero-backlash worm-gear servo reducers are specified for cyclic positioning, with sub-1 arc-minute standard backlash and ratios from 4.75:1 to 60:1 available; ratios below 20:1 are not suggested for precise reversing motion because of higher apparent backlash and lower damping.
DIN 127 split spring lock washers were withdrawn as a standard because testing showed they were ineffective at preventing bolt loosening under dynamic and even static loads, leaving DIN 6797 as the only toothed/spring washer standard still active. The parts still exist, sold as DIN 127 B or ISO 7053
Pitch differential, the radial gap between a timing pulley's pitch diameter and its outside diameter, directly controls how pitch-line velocity, tooth engagement, and backlash behave under load. For inch and metric T series it ranges 0.010–0.055 in (0.3–1.4 mm) by belt section; for AT series, 0.047–
A higher contact angle in an angular contact bearing increases axial capacity because the load line is rotated closer to the bearing axis, shifting a larger share of the applied force into the axial-load component. Standard contact angles of 15°, 25°, and 40° give progressively higher thrust ratings
A taper bush is used with a keyway to add frictional shrink-fit grip and concentricity, because a key alone cannot center the hub or absorb torque peaks without fretting, vibration, and shaft damage under shock loads.
A single-disc coupling cannot accept parallel shaft offset because one disc pack is rigid in shear; a second flex plane is mechanically required to bend in the opposite direction and complete the offset. Use a double-disc (spacer) coupling for parallel misalignment, or a single disc combined with a
A full complement ball bearing cannot carry significant thrust load because removing the cage eliminates the contact-angle control needed to transmit axial force, and adjacent balls rub against each other, generating heat and seizure risk.
Tapered roller bearings handle combined radial and axial loads because their conical rollers and matching raceways create line contact at an angle, generating reaction forces along both axes simultaneously.
Taper lock bushes are predominantly made from mild steel (often EN 1A / EN8 grades) and high-grade cast iron because the 1:12 taper geometry demands a material that machines cleanly, grips the shaft under sustained torque, and absorbs shock without brittle fracture, and mild steel is the lowest-cost
Back-to-back (DB) paired angular contact bearings resist moment loads best: the divergent contact lines widen the effective load center spacing, boosting tilting-moment capacity and system rigidity versus face-to-face (DF) or tandem (DT) pairings.
Tapered roller bearing races are most commonly machined from through-hardened chrome steel AISI 52100 (1.0% C, 1.5% Cr) for service below 120 deg C, with case-hardened low-alloy carburizing steels used for heavy-impact or large-section races per NASA TM-2012-217445.
Specify a ball spline instead of a keyed shaft when the joint must carry torque while allowing repeated, low-friction linear travel on a single shaft, or combine linear and rotary motion in one compact axis. The basic dynamic load rating of a ball spline runs 5 to 12 times that of a like-sized slide
Specify a spherical plain bearing on an oscillating pivot when loads are heavy and slow, swing angles exceed roughly 3 degrees, shock dominates over continuous rotation, or relube access is poor; a spherical roller bearing wins when the same joint must run continuously above a few hundred rpm while
Replace a rigid ball bearing with a self-aligning type when shaft-to-housing misalignment exceeds 0.5° or the application shows edge-loaded raceway wear, long shaft deflection, or field installation variability. A 6205 vs 2205 swap costs ~32% radial capacity but gains 2-3° tolerance.
A linear bearing is a cylindrical ball bushing that slides on a round, hardened shaft; a linear guide is a profiled steel rail plus a recirculating carriage block. Profiled-rail guides carry higher loads, resist moment loads, and reach sub-micron repeatability; round-shaft bearings cost less, self-a
C3 is a standardized internal-clearance suffix on a ball bearing part number, indicating radial internal looser than the CN (normal) baseline. It is the most common motor-class upgrade, used to absorb thermal expansion of the inner ring under press-fit mounting and elevated operating temperature.
AGMA service factor is a numeric multiplier (typically 1.0 to 2.5+) that increases a gearbox's rated horsepower above the application's required horsepower to absorb shock, vibration, frequent starts, and thermal stress. It directly controls gear-tooth pitting life on an 8.78 power curve, so under-s
A tapered roller bearing uses four matched parts: the cone (inner ring) carries the shaft and a thrust rib, the cup (outer ring) provides the second tapered raceway, frustum-shaped rollers transmit load through line contact, and a steel or polymer cage spaces the rollers and holds the cone assembly
Voice coil linear actuators deliver short stroke, high frequency motion in sub-50 mm travel with forces of 0.02 N to 650 N, sub-micron resolution, and bandwidths above 100 Hz for oscillation, sorting, and precision testing duties.
V-ribbed (Poly-V) belting can drive up to 20 slave rollers from a single motorized roller in live roller conveyors, with V-guide geometry for OEM pressure-roller tracking. Spec ranges span 45-77 mm widths, 656-1200 ft reel lengths, 5-inch minimum package length, and aramid tensile members for tensio
Two-row profiled linear guides suit compact, light-to-medium loads and short strokes, while four-row designs dominate heavy, high-rigidity, long-stroke automation. Decision hinges on load rating, moment capacity, speed, and dimensional envelope, not row count alone.
Tubular linear motors deliver higher speed, longer travel and zero mechanical wear, while screw-driven electric linear actuators give higher thrust density, self-locking hold and lower first cost. Pick tubular motors for >2 m/s motion, long stroke and clean rooms; pick screw-driven actuators for ver
Triple-lip sealed spherical plain bearings (suffixes 2TS, 2RS) extend grease-lubricated life in abrasive slurry service by blocking ingress at the spherical contact, with steel/steel and steel/bronze liners, bore sizes 6-300 mm per DIN ISO 12240-1.
XL profile timing pulleys use a 0.200 inch (5.08 mm) pitch, and the published Pitch Line Differential (PLD) of 0.254 mm is the constant you subtract from pitch diameter to get the outside (flangeless) diameter across the entire XL tooth range, per Pfeifer and SDP-SI engineering data.
Curvilinear timing belt profiles (HTD, GT) carry higher torque per tooth and run quieter than trapezoidal profiles, while trapezoidal profiles (MXL through XXH, T/AT) keep backlash low and cost less. Pick by torque, speed, and positioning need, not by habit.
Timing pulley PLD (Pitch Line Differential) is profile-specific, not a constant: each belt family (XL, L, H, HTD 3M/5M/8M, GT2/3/5, T2.5/T5/T10, MXL) carries its own U offset, so OD = PD − 2U only works when the correct U is paired with the tooth count and pitch. Selecting the right U by profile, th
XL-profile timing pulleys (0.200" pitch) need a Pitch Line Differential (PLD) correction, because the belt's neutral tensile-cord layer sits offset from the tooth midline, making the pitch diameter smaller than the pulley's physical center. With PLD applied, an XL 20T pulley computes to roughly 1.27
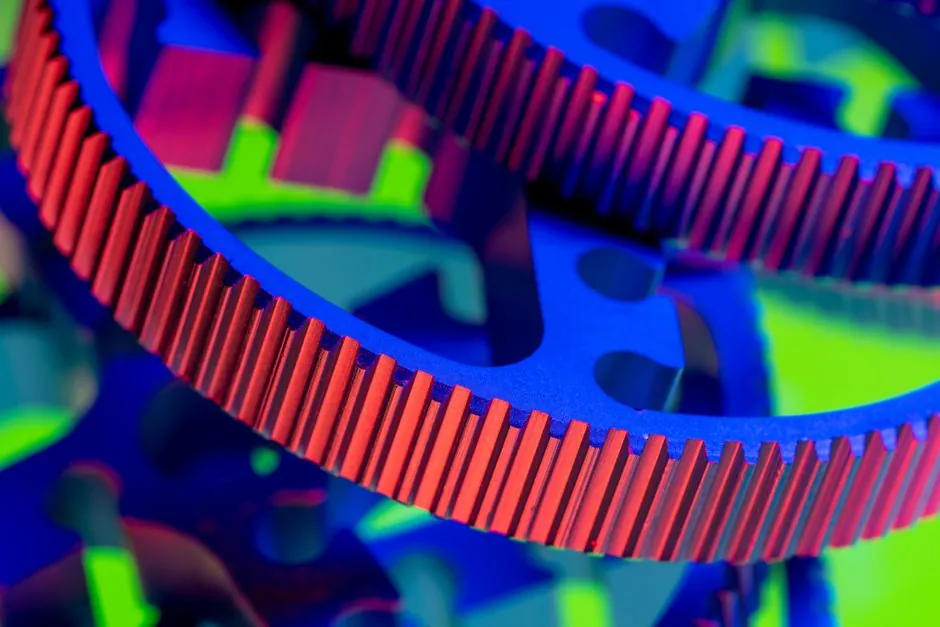
XL, L, and H are all trapezoidal imperial timing-belt profiles, distinguished primarily by pitch (0.200", 0.375", 0.500"), with proportional tooth depth, groove geometry, and torque range scaling upward. They are not interchangeable: each requires a matching pulley groove profile cut to its own stan
V-groove, timing, and ribbed pulleys are distinguished by groove geometry and tooth profile, not appearance: classical V-groove pulleys use a 40° wedge accepting A/B/C or SPA/SPB/SPC belts, ribbed pulleys run multiple micro-V grooves at fixed rib pitch (PH 1.6 mm, PJ 2.34 mm, PK 3.56 mm, PL 4.70 mm,
Telescopic multi-stage linear actuators pack long strokes into short retracted housings by nesting two, three, or four stages. Common selection metrics include retracted-to-stroke ratio, drive synchronization, and integrated feedback.
TDO (Tapered Double Outer) and TDI (Tapered Double Inner) are the two structural variants of double row tapered roller bearings, differing in which ring is the one-piece double member. TDO uses one double cup plus two cones; TDI uses one double cone plus two cups, which sets load path, mounting, and
Tapered roller bearing inch series are sold as matched cone/cup pairs identified by a hyphenated set number (e.g. LM11749/LM11710), while each half keeps its own part number for spares. Metric 30200-series sizes are encoded in a single part number per assembly and use a different naming system.
Tapered roller bearings serve two distinct roles in rotating equipment: as wheel-hub bearings handling combined radial and axial loads at low-moderate speeds, and as gearbox-shaft bearings where preload, lubrication, and arrangement (face-to-face vs back-to-back) govern service life. Selection hinge
Case-hardened steel is the recognized industry standard for tapered roller bearing races and rollers, offering roughly 40% longer fatigue life than through-hardened 52100 in shock-loaded service. For sub-100°C, steady-load applications, through-hardened 52100 remains a lower-cost option, but case-ca
A taper-lock bushing uses a shallow 8 degree tapered interface and axial bolt force to generate radial clamping pressure roughly 7x the bolt load, locking pulleys, sprockets, and couplings to shafts through pure friction, not keyways.
DIN 6885 keyways on taper-lock bushes follow the standard series width-by-bore table, but several series force a shallow DIN 6885/3 key or a non-ISO bore, and proprietary bores break interchangeability with QD hubs. Use the series, bore, and keyway cross-check before ordering.
Taper lock bushes use a standardised 1:12 taper ratio, which gives roughly 4.76° included angle and is a self-locking geometry that converts screw torque into radial clamping force on the shaft.
Taper bushing hubs convert standard jaw couplings into shaft-ready drives by mating a curved-jaw half hub with a 1108/1210/3535 taper-lock bushing. They ship as cast iron, steel, or aluminium half hubs, with applied list pricing around USD 104.68 for a 1210 size and AUD 51.66 for an L100/1108 varian
Taper Lock bushings run from series 1008 (1/2 to 1 in bore) up to 5050 (1-3/4 to 5 in bore), with intermediate sizes filling the range in fixed bore increments. QD bushings cover a wider envelope, SH at 3/8 to 1-1/8 in up to P/W/S above 12 in. Match the bushing number to the hub it must seat in, the
Taper bush jacking holes and tightening holes are separate tapped features: tightening holes pull the bush into the hub's 8° taper to clamp the shaft, while jacking holes reverse the load to eject the bush during removal. A standard 1008 to 5050 series taper lock bush typically has 2 to 3 tightening
A taper bush pulled from service should be scrapped, not reused, if the bore shows fretting, the keyway is wallowed, the split is deformed, or the taper face has corrosion pitting. Inspection takes about ten minutes and requires only calipers, a light, and a flat reference; acceptance thresholds are
Tangential (double-key) arrangements at 90 degrees suit heavy reversing flywheel loads because the second key picks up the reverse-torque reaction that would otherwise rock a single tapered key loose. Imperial flywheel keys run 1:96 taper, metric 1:100, and the hub keyway must be cut to match the ke
Tandem angular contact bearing arrangements stack two or more bearings with parallel contact lines to carry heavy unidirectional axial loads plus radial load. They are specified where thrust is single-direction only, while DB (back-to-back) or DF (face-to-face) pairs are used when thrust reverses.
For T5 and T10 timing belt pulleys, outside diameter (O.D.) is consistently smaller than pitch diameter (P.D.) and is derived as De = Dp - Hf, where Hf is the addendum height of the tooth. T5 (5 mm pitch) and T10 (10 mm pitch) share the same trapezoidal tooth family, so the same geometry rules apply
Stepper-driven linear actuators deliver 3–5% noncumulative step-angle accuracy open-loop, while servo-driven units with linear encoders reach 0.05 µm incremental motion and stay closed-loop under load. Pick stepper for cost and simplicity, servo where microns, dynamic correction, or higher speed mat
DIN 127 spring lock washers are manufactured in spring steel (per DIN 267-26), stainless steel grades A2/304, A4/316, and 316Ti, with silicon bronze, titanium, and aluminum as specialty options. Size range M2 to M100, with two end-forms (Type A tang, Type B square), intended only for property class
Stainless steel tapered roller bearings for washdown equipment are stocked in 316, 304 and 440C variants, with cone-and-cup part numbers such as SS-30205 (25×52×16.25 mm) widely available off the shelf. Choose 316 for chloride exposure, 304 for moderate washdown, and pair the unit with food-grade so
Stainless shaft keys for corrosion-resistant service are stocked from shaft diameters 6 mm through 100 mm in 304, 316, 410, 416, 17-4PH and proprietary alloys, with size mapping per JIS B 1301 and dimensions per BS 4235/ASME B17.1/DIN 6892.
Helical gears run 10-20 dB quieter and carry roughly 50% more load than spur gears of the same size, but cost 30-40% more and demand thrust bearings to handle axial thrust. The choice hinges on speed, noise tolerance, and budget constraints.
Spring washer tolerances for thickness and outside diameter are defined per series under ANSI/ASME B18.21.1 and DIN 2093 (DIN EN 16983), with 1/2" Regular split lock washers held to 0.125 in section thickness against a 0.869 in OD max. Flatness, parallelism, and material-thickness variation mus
Spring washer load-deflection curves are either linear (curved, wave, finger types, 20-90% linear range) or non-linear (Belleville/disc, governed by h/t ratio; flat safe to 1.5). Read on for selection ranges.
Spring steel and stainless steel spring washers serve the same preload function, but they are not interchangeable in corrosive service. Choose 304/301 stainless for general industrial exposure and 316 stainless (2-3% Mo) for chloride and marine environments; specify plated carbon spring steel only w
Split taper bushings allow shaft-friendly removal using jacking screws without permanent deformation, while taper-lock bushings require pulling the bushing out of the hub with progressively loosened cap screws. The choice depends on maintenance frequency, torque load, and whether the shaft can toler
Misaligned jaw couplings push spider temperature up by forcing one elastomer leg to absorb 70% of the torque at 1.5° angular misalignment, with black rubber dust and 1× shaft-speed vibration as the warning signs. Keeping angular misalignment at or below the 1° catalog limit and selecting a spider ma
Spherical roller bearings use two rows of barrel rollers rolling on a spherical raceway for high radial load at moderate misalignment (1.5-3°); spherical plain bearings slide ring-on-ring with no rolling elements, tolerating 10-15° misalignment and heavy shock loads at low speeds per DIN ISO 12240-1
Spherical plain bearings tolerate 10–15° of angular misalignment on a pivoting joint, versus roughly 0–3° for cylindrical bushings, making them the default pick when shaft-to-housing geometry cannot be held tight. Choose steel-on-steel for shock and heavy radial load, PTFE liner for dry maintenance-
Radial spherical plain bearings handle mining shock loads through sliding-contact inner/outer rings with 10-15 degree misalignment capacity, steel-on-steel or steel-on-bronze per DIN ISO 12240-1. Radial clearance targets C3-C5 in articulated joints, dump truck suspensions, and hydraulic cylinder piv
A radial spherical plain bearing is a two-ring sliding-contact unit: an inner ring with a convex spherical outer diameter mates against an outer ring with a matching concave bore, with a sliding layer (steel-on-steel, PTFE composite, PTFE film, or sintered bronze) between them. Misalignment capacity
Spherical plain bearing cross section dimensions d, D, B, C and dk are defined in DIN ISO 12240-1. Bore d, outer diameter D, inner ring width B, outer ring width C, and ball diameter dk govern interchangeability across radial series K, E, G, W.
Spacer drop-out jaw couplings let a pump be serviced by lifting the center spacer without uncoupling the hubs, cutting back-pull-out downtime. The design is a close cousin of the spacer-style grid coupling, but uses an elastomer spider, fail-safe metal-to-metal contact, and zero lubrication.
A disc coupling accepts parallel offset only when it has two flex planes, such as a double disc pack or a Thomas-style spacer; a single disc pack has zero allowable parallel offset. Per OEM data, ~0.5 mm of offset is typical for a 114.6 mm spacer at a 0.25° per-pack limit, with Oldham designs reachi
Sliding disc couplings handle turbine-shaft axial float through a floating center disc that absorbs end movement without thrust load, distinct from membrane disc designs that flex the metal. The floating-disc style suits vertical or long-span drives where limited end float must be set against sleeve
Oldham sliding disc couplings pair two metallic hubs with a non-metallic center disc, and material choice (nylon vs acetal) sets the coupling's stiffness, damping, and dimensional behavior. Acetal (POM) delivers zero-backlash, high torsional stiffness, and ~0.8% moisture absorption; nylon absorbs up
Size an elastomer jaw coupling for servo peak acceleration torque by driving the selection from the worst-case torque-time duty, not from continuous running torque, with typical service factors of 1.5-3.0 applied to peak acceleration events. Verify bore, speed, combined misalignment, and to
Single-disc (single flex) couplings accommodate angular and axial misalignment only, with Lovejoy's 8-bolt design reaching 1/2° to 1-1/2° angular capacity per pack. Double-disc (double flex) units with a spacer additionally handle parallel offset, at the cost of larger envelope, more weight, and hig
Single-row tapered roller bearings handle moderate radial + single-direction axial loads with simpler mounting; double-row (paired) units carry roughly 1.5–2x the load, accept axial force in both directions, and suit gearboxes, rolling mills, and wheel hubs. Pick double-row for heavy combined loads
Taper-lock and QD bushing tapers must be assembled dry; lubricant on the mating tapers causes hub fracture and drive slippage. Only the cap-screw threads get a light oil film before torque-up.
Parallel keys dominate general power transmission, Woodruff keys fit small and tapered shafts, taper/Gib-head keys wedge under reversing loads, and selection hinges on shaft size, direction of torque, and hub removal needs.
For high-torque shafts, match the key material to the shaft/hub steel: medium carbon steel 45C8/50C4 grade keys with hardness equal to or higher than the hub are the default per BS 4235, ASME B17.1, and DIN 6892. Stainless keys (AISI 304/316) are specified only when corrosion outweighs torque densit
For high-torque service, shaft keys should be specified in medium-carbon steel (AISI 1045 / C45) for general duty or alloy steel (AISI 4140, 4340) with UTS up to 1000 MPa for severe loads, matched to shaft hardness and governed by BS 4235, ASME B17.1, and DIN 6892.
For encoder feedback shafts, bellows and disc-style flexible couplings (zero-backlash, torsional stiffness above 1.0 N·m/deg class) are the dominant 2026 selection. Jaw couplings fit only when backlash is tolerable. Key spec gates: bore size, peak torque, parallel misalignment in inches, and max RPM
Self-aligning ball bearings tolerate 3° to 7° of dynamic angular misalignment under normal loads, while spherical roller bearings (SRBs) are typically designed for 0.5° to 2° swiveling under normal operation, expanding to 2° at low load. Both ranges are confirmed by NSK, SKF, Schaeffler, and SLF tec
Self-aligning roller (spherical) bearings carry 3–5× the radial load of self-aligning ball bearings of the same bore; ball versions run cooler and at reference speeds near 7,500 rpm, roller versions cap around 4,300 rpm. Pick SABB for light loads, high speed, and misalignment up to ±3°; pick spheric
Self-aligning ball bearings use a common spherical outer raceway to absorb ±3° of shaft misalignment, with radial internal clearance bands (C2, CN, C3, C4, C5) chosen to control thermal expansion and fit interference at mounting.
On long transmission shafts where shaft bending and mounting misalignment are unavoidable, self-aligning ball bearings (SABBs) with a spherical outer raceway handle 1.5-3° of angular misalignment at low friction and high speed, but cap radial load at roughly a quarter of an equivalent-bore spherical
Sealed pre-adjusted railway axle tapered bearing units (CTBU / TBU / CTRB) integrate sealing, factory-set clearance and pre-lubrication into a single cartridge mounted on the wheelset journal. The compact form factor shortens the axle journal, cuts friction torque up to 75% versus garter seal arrang
For disc couplings, straight-sided packs deliver the highest torque density, scalloped (contoured) packs trade torque for radial/axial flexibility, and link-type packs sit between them with modular replaceability. Pick scalloped for high misalignment, straight-sided for steady torque on aligned trai
SAE AS81820E is the U.S. aerospace standard governing self-aligning, self-lubricating spherical plain bearings, qualifying PTFE-liner designs to a 100,000-cycle performance threshold across -65°C to +250°C.
Saddle keys fit the hub keyway only and rely on friction, limiting them to light-duty low-torque drives, while sunk keys seat half-depth into both shaft and hub for positive torque transmission under higher load. For predictable slip-free duty, specify a sunk parallel or Woodruff key rather than a s
A round pin key is a circular cross-section machine key, typically a hardened dowel pin, seated half in a hole drilled into the shaft and half in a matching hole in the hub bore. It transmits torque in the 5 to 20 hp range at sub-1000 rpm applications where the shaft-hub fit is tight, but tolerates
Rotary ball splines with a built-in support bearing on the nut deliver simultaneous linear and rotary motion on a single shaft, replacing a separate user-sourced radial bearing. A linear-only ball spline transmits torque but needs an external radial bearing for any rotary motion, making the assembly
For the same bore diameter, a cylindrical roller bearing typically carries 1.5 to 2.0 times the dynamic radial load rating of a deep groove ball bearing, while ball bearings run 2 to 3 times faster and handle axial loads that would damage most roller types. Choose the family by matching contact geom
Ribbed V-belt pitch and rib height are governed by the section letter: ISO 9982 metric profiles PH, PJ, PK, PL and PM cover 1.6 mm to 9.4 mm pitch, with PH suited to small drives and PM to high-power industrial loads. Specifying a replacement belt requires three numbers: section, rib count and lengt
Stamped chain numbers decode pitch, type, strand count, and heavy-series grade. A "#40-2" mark reads as 1/2-inch pitch, standard series, duplex strand; suffixes "H" or "1"/"5" flag heavy or specialty builds.
A strain wave gear's reduction ratio is set almost entirely by the tooth-count difference between flexspline and circular spline, so jumping from 50:1 to 100:1 to 160:1 changes the package's torque capacity, torsional stiffness, and no-load running torque in ways the datasheet hides between the line
A linear guide is more than a rail and carriage: end caps, end seals, and the ball retainer each carry a defined mechanical job. This piece maps those jobs to the parts, materials, and failure modes you spec against.
Rack and pinion linear actuators routinely deliver strokes from 2 m to 50 m, with OEM payloads spanning 200 kg to 1000 kg and top speeds around 2 m/s for industrial gantry and stage builds.
The 3020 taper lock bushing has a 3.0 inch nominal maximum bore and 2.0 inch axial length, while the 2517 uses 2.5 inch bore and 1.75 inch length; the Q1 designation, in contrast, belongs to the QD bushing family, not the Taper-Lock family, and has a 1.15 inch bore ceiling at its largest size.
PreSet-style pre-adjusted wheel hub assemblies use a precision-machined spacer plus close-tolerance bearings to lock bearing spacing at the factory, removing the field endplay adjustment that the TMC RP 618 0.001-0.005 in window otherwise imposes on every wheel end.
HTD 3M, 5M, and 8M pulleys share a common circular-arc tooth profile per ISO 13050, with PLD (pitch line difference) values scaling roughly with pitch: typical 3M PLD sits near 0.280 mm, 5M around 0.480 mm, and 8M near 0.686 mm for mid-range tooth counts.
A collapsible crush sleeve sets pinion bearing preload by deforming as the pinion nut is torqued, typically 160-180 ft-lbs on Dana 30/35 axles, with rotating torque checked at 8-20 in-lbs depending on bearing condition.
For nanometer positioning, piezo actuators deliver sub-nanometer resolution and self-locking at zero power but limit stroke to hundreds of microns, while screw-driven actuators provide 10-50 mm travel with 0.05 µm minimum incremental motion at 40-70 N force. Choose piezo for sub-100 µm closed-loop o
Parallel offset capacity in a double disc pack coupling scales roughly with the spacer length between the two flex planes, because each disc pack adds a fixed angular pivot and the offset is the sum of those two pivots projected along the spacer. Doubling the spacer therefore increases allowable par
A 20-tooth XL timing pulley with a 0.254 mm pitch line differential has a pitch diameter of 30.48 mm and an outside diameter of approximately 29.98 mm, derived from (5.08 mm x 20) / 3.14159 minus the 0.254 mm PLD offset per side.
NEMA T-frame motor shaft diameters run from 0.625 in at frame 56 up to 3.375 in at 449T, with a matching square keyway scaled to the shaft. Frame size is decoded directly: first digits divided by 16 give the shaft height in inches, and the suffix letter encodes the shaft length family.
Module and diametral pitch both express gear tooth size, but module (m = pitch diameter in mm / teeth) is the ISO metric standard, while diametral pitch (DP = teeth / pitch diameter in inches) is the AGMA imperial standard, with m = 25.4 / DP governing cross-system conversion.
Miniature single-disc servo couplings with clamp hubs cover bore sizes 1/8 in to 1-3/4 in (3-45 mm) and transmit up to roughly 100 Nm, suiting stepper and small servo shafts where torsional stiffness, low inertia, and backlash-free clamp fixation matter. Aluminium-hub, stainless disc stacks (single
For small stepper axes, beam couplings win positioning accuracy and zero backlash while miniature jaw couplings win shock tolerance, vibration damping and field serviceability. Pick beam for encoders, lead/ball screws and high-resolution positioning; pick jaw for general automation where the elastom
Miniature jaw couplings sized for encoder feedback shafts (3-16 mm bores) balance backlash, torsional stiffness, and misalignment capacity. Selection hinges on spider durometer, hub machining tolerance, and servo-class wind-up limits rather than catalog torque alone.
Miniature flexible jaw couplings in the 3 to 16 mm bore range are stocked as aluminum or steel three-piece assemblies with 80 Duro polyurethane, NBR, or Hytrel spiders, rated roughly 0.7 to 130 Nm with bores to 16 mm. Standard L, XO, MJC, and L090 sizes cover stepper, encoder, and small servo drivet
Miniature ball splines with 4-8 mm shaft diameters deliver basic dynamic load ratings from roughly 200 N to 3,500 N across THK, NB, HIWIN, and Thomson ranges. Stainless variants, retainer designs, and torque capacity drive selection for compact robotics, medical, and semiconductor axes.
Metal scrapers and double-seal upgrades on linear guide blocks are non-contact wipers that clear large debris above 0.3 mm and stacked lip seals that retain grease against fine particulates, respectively. Choose them for machine shops, woodworking cells, and foundries, and skip them in cleanrooms or
For a gearbox input shaft, key size is selected from shaft diameter using DIN 6885-1 / ASME B17.1 tables, then verified with bearing and shear checks at 90-120 MPa allowable bearing pressure. A half-key mock-up is mandatory for rotors balanced to ISO 21940-32:2012 grade G2.5 or finer.
Hydraulic tensioner assembly leaves a bolted joint free of torsional twist, so the only torque that locks the eccentric fixed tensioner's locknut against vibration is the nut-factor friction on the thread flanks and the washer face, typically sized for K=0.18–0.20.
Friction-locked locking assemblies transmit torque via 360-degree radial pressure from tapered thrust rings, eliminating keyway notch stress, while keyways rely on single-line shear at the key flanks. Spec range spans 270 Nm to 2.4 million Nm across Ringfeder RfN 7012 series, suiting loads that exce
Roller-type linear guides typically deliver 30% to 50% higher load capacity than ball-type equivalents in the same size class, with line contact instead of point contact driving the gain. Ball guides remain the default for general automation up to 1-3 m/s; roller guides are specified when load, rigi
Linear ball spline systems combine a grooved shaft and a recirculating-ball nut to transmit torque and linear thrust on one axis, with basic dynamic load ratings 5 to 12 times a like-sized slide bush and torque capacities engineered via gothic-arch (4-point) or circular-arc (2-point) raceways.
Ball spline preload is sold in 2-3 standardized classes (Z0/light, Z1/low, Z2/medium) with light preload typically about 2% of basic static load rating, reducing angular backlash in torque transmission.
Linear ball bearings (μ ≈ 0.0010–0.0030) deliver 10–100× lower friction than plain sleeve bushings (μ ≈ 0.05–0.20), but sleeve bushings can cost roughly a tenth as much, absorb shock better, and tolerate contamination. Choose rolling elements for high-speed continuous duty; choose plain sleeves for
Bronze plain linear bearings out-carry linear ball bearings by roughly 46:1 on static load (100,500 lb vs 2,165 lb) per PBC Linear's 2025 spec table, at the cost of a 5x higher coefficient of friction and ~2x lower top speed. Use bronze bushings for shock-loaded, dirty, low-precision moves; pic
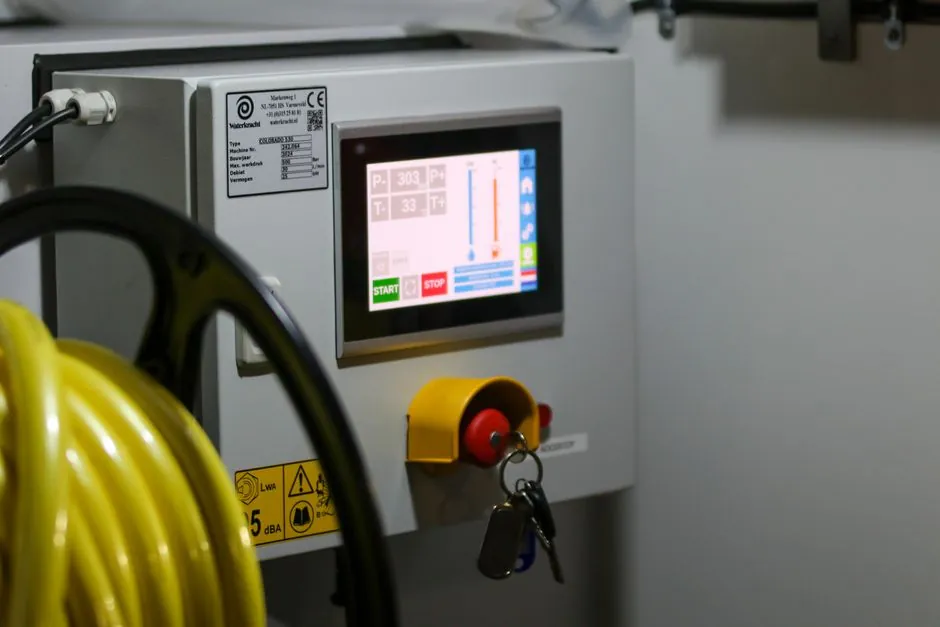
Linear actuators with 1000 mm stroke are widely stocked off-the-shelf across 12V/24V, 750N to 6000N load ratings, with custom strokes between 10 mm and 2000 mm available. Above 1000 mm, ball-screw critical speed forces a switch to belt drive or larger-diameter screws.
Linear actuators are usually specified by S3 intermittent periodic duty (a percentage on/off), while S2 short-time duty is a single fixed run duration (e.g. S2 30 min) followed by a full cool-down to ambient. Choose S2 for hoists, gate drives, and one-shot positioning strokes; choose S3 for repeated
IP66-rated linear actuators are sealed to IEC 60529 for total dust ingress and 100 L/min water-jet exposure, suiting outdoor, marine, and most washdown jobs. For hot caustic daily washdown or submersion, step up to IP68 or IP69K, since IP54/IP65 typically fails under those conditions.
For continuous-duty machine builds, 100% rated linear actuators with servomotors are the only safe pick; standard 25% units are limited to ~2.5 min run per 10-min window and will fail prematurely if pushed past that thermal limit.
Line-contact roller bearings carry roughly 4-7x the dynamic load of comparably sized point-contact ball bearings, at the cost of lower speed (0.5-1.5 m/s vs 1-3 m/s) and higher friction (μ 0.003-0.008 vs 0.002-0.004). Selection hinges on contact geometry, Hertzian stress, and the load-versus-speed t
For centrifugal pump drives up to roughly 1 hp and 3600 rpm, specify a jaw coupling with a 92 Shore A spider when misalignment stays under 1° and 0.4 mm. Choose a tyre coupling when shaft separation exceeds the jaw coupling's axial limit, ambient temperature drops below -30 °C, or shock loads domina
Jaw couplings span a continuous size range from roughly 0.4 Nm (3.5 in-lbs) miniature units for encoders and small pumps up to 19,209 Nm (170,004 in-lbs) heavy-duty curved-jaw units for pumps, compressors, and conveyors, with bore diameters from 4.45 mm to 178 mm. Selection is governed by design tor
Industry practice for jaw coupling hubs calls for shaft engagement equal to at least the shaft diameter, with the Lovejoy L-Line installation guide stating hub engagement on the shaft should equal the shaft diameter, and SKF coupling documentation flagging any case where the calculated minimum requi
Jaw coupling alignment with a straightedge and feeler gauge is the lowest-cost precision method: set four contact readings at 12, 3, 6, and 9 o'clock, then shim or slide the driver to keep offset below roughly 1-3 mils and angularity under 0.5-1.0 mil/inch. The technique is limited to roughly 1,800
Jaw couplings accept angular, parallel, and axial misalignment through their elastomeric spider, with field targets around 0.5 mils/inch angular and 2 mils (0.002 in) parallel offset at speeds up to 3600 RPM, per current engineering guidance.
ISO 6336 and AGMA 2001 compute gear load capacity through similar stress-vs-allowable frameworks, but the two standards diverge on geometry, load-distribution, and safety-factor treatment, often yielding noticeably different ratings on the same gear pair.
ISO 5294:2012 governs inch-pitch synchronous belt pulleys (MXL, XXL, XL, L, H, XH, XXH) with involute or straight-sided teeth, fixed pitch-to-pitch tolerances, and preferred diameter and width tables. Specifying MXL or XL stock pulleys per this standard gives interchangeability with ISO 5296-1 belts
ISO 17396 specifies metric-pitch synchronous belt drives with T and AT trapezoidal tooth profiles for power transmission and indexing. ISO 17396:2014 is withdrawn and replaced by ISO 17396:2017 (also withdrawn, revised by ISO 17396:2024). Specifiers use it together with ISO 13050 for curvilinear pro
Internal (ring) gears deliver 20-50% higher torque than equivalent external gears via convex-concave contact, at the cost of shaping-only manufacturing and a 30-40% higher part price. Choose internal for planetary, robotics, and aerospace compact drives; choose external for parallel-shaft reducers a
Inconel 718 disc springs rated for continuous 500°C service use precipitation-hardened Ni-Cr-Nb-Mo stock, retain roughly 75% tensile strength at 700°C, and require NACE MR0175 heat treatment for sour service. Selection hinges on spring series, deflection ratio, and stress-relaxation limits, not just
Imperial taper-lock bushings (1008 through 5050) cover inch shafts from 1/2" to 3-7/8" with ANSI B17.1 keyways ranging 1/8"×1/16" to 3/4"×3/8". Standard fractional bore increments and parallel keyseat pairing govern selection; sizes above 5050 break to a metric-only family to 120100.
IEC motor shaft end key and keyway dimensions are standardized by frame size, with frame 80 typically using 19 mm shafts and 6x6 keys, frame 132 using 38 mm shafts with 10x8 keys, and frame 315 using 80 mm shafts with 22x14 keys per IEC 60072-1.
A ball bearing designation decodes in three parts: first digit = bearing type, second digit = dimension series (width/OD), last two digits = bore in mm (×5 above 10 mm). Reading 6206 gives type 6, series 2, 30 mm bore.
Radial ball bearing inner rings on a rotating shaft are typically installed with an interference fit in the j5 to m6 range, while the stationary outer ring uses a loose H6/H7 housing fit. Tightness scales with load severity, and ABMA Standard 7 governs metric series fits.
Spindle angular contact bearings need only a small factory preload (light or extra-light class) to remove internal clearance, typically producing 2x to 3x rigidity gain. The exact preload force is set by race grinding at the bearing maker, then carried into the spindle via ground spacers or a measur
A 12V linear actuator typically draws between 2A and 12A at full rated load, with a 400 lb unit commonly hitting 12A and a lighter 150 lb load on the same unit dropping to about 7A. Startup surge can spike to 5x the running current, so a properly sized DC supply should carry 1.25x to 1.5x headroom o
Standard ball splines use 2 to 6 ball tracks on the shaft, with 4 tracks the most common configuration; a 3-track gothic-arch design yields 6 contact rows. Track count directly governs load capacity, moment rigidity, and recirculation geometry.
Outside diameter of a timing pulley is found by subtracting twice the belt's tooth depth U from the pitch diameter: OD = PD - 2U, where PD = (pitch x tooth count) / pi and U is the cord-to-tooth-tip distance for the chosen pitch profile.
Gear ratio equals the number of teeth on the output (driven) gear divided by the number of teeth on the input (driving) gear; the tooth thickness and spacing cancel because meshing gears must share the same module and pressure angle. The same rule extends to compound gear trains by multiplying stage
Tapered roller bearing preload is set during installation by adjusting the axial clearance between cone and cup, typically via shims, spacers, or a torque-controlled nut, to a few thousandths of an inch. Methods include manual feeler-gauge setting, shim stacking, and matched-spacer pairs (O, X, or t
Self-aligning ball bearings compensate for shaft misalignment through a common spherical outer raceway that lets the inner ring and twin ball rows pivot around the bearing's center, typically absorbing 2 to 3 degrees of angular misalignment.
Use a disc coupling selector chart by computing design torque (HP x 9550 / RPM, multiplied by service factor), locating the torque row at your operating RPM on the chart's power/speed grid, and then verifying bore range, DBSE spacer length, angular/parallel/axial misalignment limits, and torsional s
Sizing a gearbox for a belt conveyor drive starts with calculating the steady-state belt pull, converting that to torque at the drive pulley, applying a 1.5 to 2.0 service factor, then matching gearbox output speed and ratio to a standard 1750 RPM or 1450 RPM motor. Two-stage or three-stage helical
For a centrifugal pump driven by an electric motor, a flexible elastomeric coupling (EPDM, neoprene, or urethane insert) is the default choice below ~7.5 kW at 1,750–3,600 rpm; spec selection starts from service-factored torque, then bore, DBSE, and misalignment envelope.

Identify a timing pulley profile by dividing the tooth count by 10 for a quick 8 mm pitch O.D. estimate, then confirm pitch (5.08 mm XL vs 5.00 mm 5M), profile shape (trapezoidal MXL/XL/L/H/XH/XXH vs HTD 3M/5M/8M/14M vs GT2/GT3), width, and tooth count before ordering a replacement.

Linear actuator duty cycle is calculated as run time divided by total cycle time (on-time plus off-time) multiplied by 100, with a 10-minute reference window. A 20% rating permits 2 minutes of operation per 10 minutes before mandatory rest to dissipate motor heat.

Hollow-shaft strain wave gear units route cables, air lines and laser beams through the gear's central bore, eliminating external cable management on multi-axis robots. Rated torques span 10 Nm to over 7,000 Nm across 1 arc-min zero-backlash designs, with bore diameters scaled to the frame size.

Elastomer jaw couplings transmit torque through a star-shaped polyurethane or rubber spider compressed between two hubs, with torque ratings up to 525 N·m and 1° angular / 0.4 mm parallel misalignment tolerance. Selection pivots on hub precision (cast vs machined), spider durometer, and ope

Heavy-series radial spherical plain bearings sized for boom-pin pivots on mobile equipment pair a wider outer ring with case-carburized or through-hardened steel sliding surfaces, carry alternating heavy radial load plus shock, and conform to DIN ISO 12240-1 dimensional series E and C. For high-shoc

Strain-wave harmonic reducers deliver single-stage ratios from 30:1 to 160:1, peak torque ratings spanning 450 in-lbs to 60,500 in-lbs, and zero-backlash accuracy across cup and shaft configurations for servo and stepper applications.

Hall and optical encoder feedback both deliver digital pulse trains to electric linear actuator controllers, but Hall magnetic sensing handles contamination and -40°C to +150°C, while optical encoders deliver 0.1° accuracy at 1,024-65,536 PPR for precision throttling.

H-type taper lock bushes use a 4-bolt, twin half-shell design for higher torque, while F-type taper lock bushes rely on a 2-bolt, single split with a nominal 8° taper. Both mount via blind hex screws, but H-pattern screw spacing and the extra clamping surface give H-types roughly double the bore ran

Full complement (cageless) roller bearings carry roughly 20% to 40% more radial load than equivalent caged designs, but their limiting speed drops by an order of magnitude and friction rises because of roller-to-roller contact. Pick full complement for slow, heavy radial work; pick caged for anythin

Formed (swaged) radial spherical plain bearings cold-form a ductile race around a hardened ball for high static load and 80–100% contact area, while machined (loader-slot) bearings fully machine and case-harden the race for moderate-motion, replaceable-ball service. Choose formed for heavy static or

Flexible disc couplings balance high-speed turbomachinery trains through all-metal, torsionally stiff disc packs (typically 0.4-1.0 mm shims, 4-12 deep) that hold every component rigidly on the rotational axis, with API 671 governing design for refinery and compressor service.

Fixed tensioners lose effective tension under load, while spring-loaded automatic tensioners maintain wrap angle and reduce belt wear. Choose spring-loaded units for high-torque accessory drives and fixed units only for low-load applications.

Screw-retained feather keys are the standard mechanism for axially sliding gears, with a tight press fit in the shaft keyway and a clearance fit in the hub keyway. One or two socket head cap screws through the key body lock it to the shaft, allowing controlled hub travel while transmitting full torq

European standard DIN EN 16983 has fully replaced German-only DIN 2093 since 01.02.2017 with identical technical content, governing disc spring quality, dimensions, and tolerances across groups 1-3 by material thickness.

For jaw-type couplings, 92 ShA and 98 ShA spider elements differ in a clear trade-off: 92 ShA gives better vibration damping and electrical isolation, while 98 ShA carries higher torque and runs hotter, with 80 ShA and 64 ShD options outside this pair for specialized duty. Selection is driven by dri

Double-row self-aligning ball bearings (SABBs) and double-row spherical roller bearings (SRBs) both compensate for shaft misalignment but diverge sharply on load, speed, and axial capacity. A 60mm-bore SABB (1212) carries 25.5 kN dynamic load at 7,500 rpm, while an equivalent SRB (22212E) carries 12

Double disc couplings handle angular plus parallel misalignment through two flex planes, while single disc packs cover angular and axial only. Pick double for parallel offset or thermal growth; pick single for tight, close-coupled, angular-only service. Misalignment budget, API-610 balance class, an

Operating a linear actuator at 50% of rated load does not double its duty cycle, but it does extend allowable run time by roughly 20-30% in standard DC actuator designs. Higher mechanical load increases motor current and internal heat, reducing duty cycle; lighter load and lower speed let the unit s

Linear ball bearings require external grease or oil lubrication; linear plain bearings (PTFE-lined, polymer, oil-impregnated bronze) are designed to run without external lube via material transfer or embedded solid lubricants.

A DLC-coated ball bearing does not eliminate grease by default: a-C:H DLC still needs grease in most industrial service, while highly hydrogenated DLC (~50 at% H) can run dry in vacuum or inert gas. Coat thickness is held to 5 micrometers maximum via PVD or CVD to preserve bearing geometry.

DIN 2093 disc spring (Belleville) dimensions span bolt sizes M4 to M250, with outer diameters from 8 mm to 250 mm, three manufacturing groups split at 1.25 mm and 6 mm thickness, and standard Series A tolerances of h12 on O.D. and H12 on I.D..

Parallel-stacked disc springs lose 2–3% load per sliding interface to friction hysteresis, and that gap between loading and unloading curves is exactly what gives them damping value in shock-absorbing service.

DIN EN 16983 fatigue life diagrams for disc springs rely on tensile stress at points II and III, with three thickness groups: under 1.25 mm, 1.25–6 mm, and over 6 mm. Standard rule of thumb: preload ≥15%, maximum deflection ≤75%, and stacking in parallel can reduce life through heat buildup. Example

Disc pack bolt count drives a direct torque-versus-misalignment trade-off: 4-bolt packs balance both and dominate general pump/motor duty, 6-bolt packs add torque density with modest misalignment loss, and 8-bolt packs maximize torque but cut angular capacity. Pick on duty cycle, peak torque, and IS

Disc coupling catalogues publish a continuous rated torque per size, but allowable peak torque is a manufacturer-specific value tied to disc pack geometry, bolt count and fatigue life. Selecting by rated torque alone is unsafe; peak, reversing and service factor must be checked on the same family da

Disc coupling rated torque is set by disc pack size, not by bore. A Lovejoy SX 185-6 is 29,205 in-lb nominal (58,410 in-lb peak) regardless of bore. Bore only sets the shaft fit envelope and the torque ceiling imposed by the key, hub length, and taper-lock bushing capacity, with TB Woods sizing

Disc coupling size charts span roughly 0.1 to 12,000 Nm nominal torque, mapping small servo bores (3 to 19 mm) to large pump-shaft bores up to 165 mm. Selection is driven by bore, torque with service factor, speed, and misalignment budget, not by outer diameter alone.

DIN EN 16983 (formerly DIN 2093) splits conical disc springs into three manufacturing groups by material thickness t: Group 1 below 1.25 mm, Group 2 from 1.25 to 6 mm, and Group 3 over 6 mm up to 14 mm, with contact flats and reduced thickness permitted only on Group 3. Group also fixes production r

DIN EN 16983 (formerly DIN 2093) lets disc spring free height lo exceed the published tolerance when needed to hit the spring force at the test deflection (lo - 0.75 ho), with force deviation bands tightening from +25%/-7.5% in Group 1 to +/-5% in Group 3 above 6 mm thickness.

DLC-coated ball bearings run dry in vacuum where grease outgasses, with hydrogenated a-C:H (PACVD) and ta-C variants delivering μ 0.008-0.1 and 1000-4000+ HV hardness; expect 2-4 μm film thickness, hydrogen-free grades for high-vacuum, and steel-cage DLC options for cryopump, space-mechanism, and se

CuSn12, CuSn12Ni2, and aluminum bronze (CuAl10Fe3/CuAl10Fe5Ni5) cover most industrial worm wheel specs; CuSn12Ni2 is the workhorse for general sliding wear, CuSn10P1 sits below it on load, and the aluminum bronzes are picked when shock load, abrasion, or seawater exposure dominate the duty cycle.

Curved-jaw (zero-backlash) jaw couplings are a three-piece hub-and-spider design whose radial jaw crown press-fits the elastomer to remove rotational play, while straight-jaw units keep the traditional trapezoidal profile and accept more misalignment at the cost of measurable backlash. The choice hi

Match conveyor gearbox selection to torque and belt speed: compute drive-shaft torque from total belt pull and pulley radius, apply a 1.5–2.0 service factor, then choose helical, planetary, worm, or bevel units by ratio, mounting, efficiency, and ambient rating. Rule of thumb: rated torque at least

Conrad deep-groove ball bearings take both radial and axial loads but are geometrically limited to roughly 50% of the theoretical full ball complement, capping load capacity. Full-complement designs gain up to 45% higher dynamic and static load ratings, but pay for it with roughly an order-of-magnit

Tapered roller bearing setting is established at machine assembly by axially locating one bearing row against its opposing row, choosing end play, line-to-line, or preload based on load zone width. Timken's published techniques cover manual shim, torque, Acro-Set, Projecta-Set, Set-Right, and preset
Specifying a complete disc coupling assembly versus a disc-pack-only replacement is a cost-versus-traceability decision: pack-only swaps are cheaper and faster on standard SX/DI styles, while full center-member replacement is mandatory on split-spacer SXCS/SXCST designs and on any coupling showing f

Silicon nitride balls measure about 1,400 HV, roughly double the 600-700 HV range of chrome steel balls, giving Si3N4 a clear hardness edge but lower fracture toughness. The pick is Si3N4 for high speed, high heat, and corrosion exposure; chrome steel remains the lower-cost default for general-purpo

ANSI #40, #60, and #80 roller chain are defined by ASME B29.1-2011 pitch values of 0.500 in (12.70 mm), 0.750 in (19.05 mm), and 1.000 in (25.40 mm), with minimum tensile strengths of 3,970 lbs, 9,270 lbs, and 16,540 lbs respectively. Selection is driven by pitch compatibility, working load, and req

Case-hardened ground worm shafts (58-64 HRC, 0.5-2.0 mm case) suit high-speed sliding contact and precision gearboxes, while through-hardened worms (28-42 HRC core, uniform hardness) fit heavy, shock-loaded, large-diameter applications. Choice is set by load profile, distortion tolerance, module siz

Yes, ball splines accept radial loads perpendicular to the shaft axis, but torque transfer is their primary design purpose. Grooved-shaft contact geometry lets them also resist moment and overhung loads up to roughly twice what comparable linear bushings handle.

A linear solenoid can replace an electric linear actuator for a 20 mm stroke only when the load is light, the duty is intermittent, and binary on/off motion is acceptable, because solenoids top out around 5-20 mm stroke and 5-120 N force.

For precision servo axes, bellows couplings deliver torsional stiffness of roughly 10,000-30,000 Nm/rad on a 25 mm OD unit, beam couplings sit in the 200-2,000 Nm/rad elastomer-dependent band, and Oldham couplings occupy a medium tier around 500-2,000 Nm/rad with a 10,000-100,000-cycle acetal-center

For encoder shafts, beam (helical) couplings are the lower-cost, higher-compliance choice (5° angular, 0.010 in parallel, 0.010 in axial, torque 1.2-100 lb-in), while metal bellows couplings deliver higher torsional stiffness and speed (up to 52,000 rpm, 3098 lb-in) for precision motion control. Pic

Ball spline shafts are routinely manufactured in lengths up to 2 m, with SNR/NTN BSP series covering solid and hollow shafts from 4 mm to 100 mm diameter, while 4-groove gothic-arch raceways deliver 5-12x the dynamic load rating of an equivalent slide bush.

Ball spline shaft deflection under radial load is solved with beam-bending equations keyed to support conditions (both ends free, both ends fixed, cantilever), using geometric moment of inertia I and the manufacturer's E modulus of 2.06×10^5 N/mm².

Ball screws reach 90% or higher mechanical efficiency while lead screws sit around 20% to 40% on the same duty; back-driven ball screws need a brake, lead screws do not. The right pick is a four-axis call: efficiency, backlash, duty cycle, and self-locking.

A combined ball-screw-and-ball-spline shaft on a SCARA robot Z-theta axis merges vertical lift and end-of-arm rotation on a single shaft, cutting part count, footprint and alignment work versus dual-shaft designs. The architecture is dominated by a rotary ball spline: grooved shaft for Z travel, int

Caged (ball retainer) linear guide blocks trade ~10-20% dynamic load capacity for cooler running, lower noise, and longer grease life versus full-complement blocks. Choose caged for high speed, clean rooms, and frequent block removal; choose full-complement for maximum static load in a given block s

Dynamic load rating C and static load rating C0 are not interchangeable on a ball bearing datasheet. C governs fatigue life during rotation per ISO 281:2007; C0 governs permanent brinelling at standstill per ISO 76. Mixing the two typically wastes material, since a 25% overload cuts L10 life by roug

Metric deep groove ball bearing dimensions follow ISO 15:2017, with bore × OD × width coded into the part number; the 6200, 6300, 6000, 6800, and 6900 series cover 10-50 mm bores and are the default reference when matching a shaft and housing.

Back-to-back (DB / O arrangement) and face-to-face (DF / X arrangement) angular contact bearing pairings differ primarily in effective load centre spacing, which dictates moment-load capacity versus axial thermal growth tolerance. DB sets a wider effective span and resists tilting forces, while DF p

API 671 specifies a 1.5 service factor on nominal torque for disc couplings in turbomachinery; for general machinery, multipliers of 2.0-2.5 cover conveyors and heavy冲击 loads, and the resulting rated torque becomes the selection floor.

ANSI B17.2 Woodruff key numbers encode two dimensions: the last two digits are the nominal diameter in eighths of an inch, and the preceding digits are the nominal width in thirty-seconds of an inch. So #606 is 6/32 (3/16") wide on a 6/8 (3/4") diameter, and #808 is 8/32 (1/4") wide on 8/8 (1") diam

ANSI B17.1 governs inch-series parallel keys and keyseats up to roughly 6.5 in shaft diameter (square keys preferred), while ISO 773 (with DIN 6885/1) governs metric parallel keys from 6 to 500 mm. The two systems are dimensionally equivalent in intent but not interchangeable: a 25 mm shaft takes a

For high-speed machine tool spindles, angular contact bearing preload sets the trade-off between stiffness and heat: light/extra-light factory preload, applied in a back-to-back duplex and verified by drag torque, is the dominant spec for precision CNC rebuilds.

Angular contact ball bearings are offered in three stock contact angles: 15°, 25°, and 40°. The 15°–25° range is optimized for high-speed spindles and combined radial-heavy loading, while 30°–40° contact angles trade speed for higher axial load capacity and stiffness.

For a single gearset, AGMA 2001-D04 and ISO 6336 commonly return different torque and power ratings, with ISO typically yielding the higher number for the same geometry and material. Use both standards together, run the geometry through each, then verify the gearbox against API 613/617/672/677 if th

AGMA service factor is a load-severity multiplier used to size gearboxes: SF = rated capacity / required power, with Class I = 1.00, Class II = 1.41, Class III = 2.00 per AGMA 6013 for a 10-hour baseline. Real applications require a composite SF (load x duration x starts x temperature) because a sin

For disc springs (DIN EN 16983), C75S (Ck75, 1.1248) suits thin sections up to about 2-3 mm where its cost and availability dominate, while 51CrV4 (1.8159) is specified for thicker discs and any application requiring higher hardenability, better through-thickness strength, and longer fatigue life at

For most single-load-direction automation builds, a 4-track gothic-arch ball spline is the higher-load-capacity-per-bulk choice, rated roughly 5-12x a like-sized slide bushing. Pick 6-track only when combined radial + moment load vectors and moment stiffness justify the larger nut envelope and

For key stock and shaft components, 303 stainless delivers higher tensile strength (around 620 MPa) and superior machinability thanks to its 0.15% sulfur addition, while 316 stainless trades a small strength reduction for 2-3% molybdenum content that resists pitting in chloride and marine environmen

DIN 137 A and DIN 137 B spring washers stamped from 1.4310 (AISI 302) austenitic spring stainless are functionally identical to A2 stainless spring washers, since A2 is the ISO 3506-1 grouping for 1.4310 chemistry with 500-700 N/mm² tensile and service to 300 °C. Pick 1.4310/A2 for non-marine, non-c

0.250" x 0.250" square key stock is a standard ANSI B17.1 Class 2 cold-drawn medium-carbon keystock size, typically stocked in 12" to 36" lengths and conforming to ASTM A29 material spec. Standard tolerance bands include nominal, oversize (+0.002"/+0.003"), and undersize (-0.001"/-0.002") for class

A 0.250 x 0.250 inch square key on a nominal 1 inch shaft carries a width/height tolerance band of 0.249 to 0.252 in per BS 46 Part 1:1958, with length selection per IS 2048:1983 and fit class per ANSI B17.1.

Lock nut selection for textile mills hinges on vibration severity, corrosion exposure, and reusability: nylon-insert, all-metal prevailing-torque, and jam-nut pairs each solve a different loosening mechanism found in spinning, weaving, and finishing equipment.

Universal joint selection for pulp and paper mills is governed by five spec-driven criteria: misalignment angle, torque and shock loading, lubrication class, material/environmental resistance, and bore-keyway sizing. Electric-motor driven lines can run below the common 3 degree minimum, with low-ang

Marine universal joint selection is governed by operating angle, torque, RPM, shaft misalignment type, and corrosion exposure. Match MIL-20625A or MIL-J-6193 specs, 30° max angle, and ductile iron or stainless bodies for saltwater service.

Locking assembly selection in pulp and paper mills is driven by shaft diameter, transmissible torque, axial displacement tolerance, and corrosion resistance. Self-centering and low-surface-pressure series suit refiner and dryer drives where moisture, chemicals, and shock loads dominate. The right se

Universal joint selection for wind turbine drivelines centers on operating-angle, torque-density and bearing-life trade-offs, with Cardan/Hooke joints typically limited to ~45° single-joint angles and 15°+ misalignment advantages over gear couplings under high-torque, low-maintenance duty.

V-belt selection for mining drives comes down to four picks: classical A/B/C/D/E profiles for legacy equipment, narrow cross-sections for high-power density, wrapped or raw-edge construction matched to ambient temperature, and a service factor of 1.4-1.6 for dusty or shock-loaded crusher and conveyo

Steel-mill V-belt selection hinges on Design Horsepower (motor HP x service factor 1.3-1.8) and sheave compatibility, with classical C/D/E or narrow 5V/8V sections dominating heavy-duty drives. Cogged raw-edge or wrapped constructions are specified where heat, shock load, or small-diameter sheaves f

For material handling conveyors, select single universal joints only for angles ≤45° with low-to-moderate speeds; specify double-joint or telescoping drive shafts for up to 90° combined angles, parallel offset, or constant-velocity needs. Match alloy-steel bodies to high-cycle torque and stainless o

For wind turbine drivetrains, two-piece clamp collars in 303/316 stainless or zinc-plated steel are the default pick: they deliver roughly twice the axial holding power of a set-screw collar, can be installed on an already-mounted shaft, and survive nacelle humidity when face-to-bore TIR stays under

Needle-bearing single universal joints dominate packaging-line drives for their low friction at 300-1500 RPM, with double joints reserved for shafts exceeding 45° misalignment. Selection hinges on torque, angle, lubricant seal, and stainless options for washdown.

For marine duty, specify ANSI Type B/C roller chain sprockets with at least 17 teeth, 17-21 tooth small pinion ratio, hub-side-toward-bearing mounting, and 316 stainless or surface-hardened steel per ANSI B29.1-1975 to resist salt corrosion.

Cardan universal joints remain the most efficient spindle option for steel rolling mills, handling 15°+ misalignment, up to 553,000 Nm torque, and cutting chatter-related surface defects on 5-stand cold mills.

Mining bolt joints face dynamic vibration, shock loads in the 4.5–22.2 kN hold-down range, and abrasive contamination, so spring washer selection in 2026 hinges on matching Belleville, wave, or split-lock geometry to load class, material to corrosion exposure, and stacking to required working range.

For textile mills, conveyor chain selection pivots on three hard rules: low-speed to moderate-speed operation (typically under 200 ft/min), strict lubricant containment to avoid product contamination, and chain type matched to load, lint, and humidity conditions on the line. Use roller chain baselin

A lock nut is selected by thread standard and size, base material, locking mechanism (nylon insert, all-metal deformed thread, prevailing-torque ribbed, or castellated/crown), corrosion class, and reusability. Match these to vibration, temperature, and chemical exposure; for a one-time high-vibratio
Locking assemblies (locking elements for shaft-hub connections) deliver zero-backlash torque transmission, easy mounting/dismounting, and repeatable reassembly, but introduce higher unit cost, concentricity sensitivity, and surface-pressure limits that engineers must weigh per ISO fit and DIN tolera

Helical gear reducers for semiconductor tools are specified at ≤5 kNm torque, low-backlash (≤3 arcmin) helical-bevel or coaxial units with food-grade or epoxy-paint housings, not the >10 kNm cement-mill units dominating the 2026 catalog listings from Renold, I-MAK, Sumitomo, Galbiati, FIMET and Siti
Chinese slewing ring bearing supply in 2026 is anchored in three regional clusters — Xuzhou, Luoyang/ma'anshan and Wuxi — with bore ranges from 200 mm to 5000 mm and OEM single-row external-gear units quoted at US$365–421 FOB per piece on Made-in-China as of 2026-05-27.
Slewing drive installation hinges on a flat, rigid mating flange, a bolt pattern torqued in a star sequence, and a worm/wormwheel mesh check; misaligned mounting surfaces are the single most common cause of premature gear wear on solar trackers, cranes, and small wind turbines.

Self-lubricating PTFE-lined spherical plain bearings (GE..FW-2RS, 100Cr6 steel/PTFE) are the dominant spec for data center swing-link and tilting-frame pivots, where maintenance access is restricted and ambient holds 20-30°C. Spec selection hinges on radial static load, pivot angle, and ball materia
Bucket elevators and conveyor chains both move bulk material, but a bucket elevator is built for vertical or steeply inclined lifts (up to 40–80 m) while a conveyor chain drives horizontal or low-angle enclosed conveying. Selection turns on lift height, temperature, material abrasiveness and through
Belt tensioner price in 2026 spans roughly USD 10 for an aftermarket V-ribbed pulley to over USD 239 for an OEM Mopar assembly, with industrial spring-loaded units and truck-grade MOQs around 100 pieces set on top of that automotive range.

Stainless steel 304/316 and engineered polymer roller bearing designs dominate food processing selections in 2026, prioritising corrosion resistance, cleanability, and NSF/food-grade lubrication over standard grease-packed steel units.

Belt conveyor systems are split into bulk-material and unit-handling families, with flat, troughed, cleated, magnetic, and pusher variants selected against load profile, incline, and abrasion class. Selection pivots on belt width (300–2400 mm), belt tensile rating (EP 315–EP 2500), and idler trough
A slewing ring bearing is a rotational rolling-element bearing sized for heavy, slow-turning or slow-oscillating loads on platforms like cranes, excavators and aerial work platforms; selection is driven by rolling element type, gear option and dimensional envelope rather than by speed rating.
Linear guide rail FOB China ranges from roughly US$159 per unit for small-format crossed-roller rails to US$1,150–1,600 per ton for raw U/C-channel steel guide stock, with ball-rail assemblies typically US$15–800+ per block/rail set depending on size, accuracy class and preload.
Chinese OEM-supplied taper-lock bushes for SPB pulleys, sprockets and gear hubs are listed on Made-in-China and Alibaba at roughly US$5–30 per piece at 1-piece MOQ as of Q2 2026, with GG25 grey cast iron and ISO 9001-certified ductile variants dominating the catalogue.

Food-grade ball bearing selection pivots on four pillars: 300-series stainless or PEEK/PTFE components, H1 food-grade lubricant, IP66+ sealing, and documented compliance with FDA 21 CFR / EC 1935/2004 for incidental contact zones.

Conveyor chain installation hinges on tensioning, sprocket alignment, and take-up travel: most drop-forged and welded-steel lines accept 1-3% elongation at break, so pre-load to within 1-2% of rated working load. ANSI/ASME B20.1 governs mechanical-conveyor safety in the US, while ISO 9001 factories
Retaining rings and shaft collars both axially locate components on a shaft, but a retaining ring is a sprung steel fastener that snaps into a groove and takes only thrust load, while a shaft collar is a solid ring clamped to the shaft by a setscrew or clamp action and can carry thrust, torque, or b

Angular contact bearings for pulp and paper machines are typically specified as paired duplex sets with 25° to 40° contact angles, phenolic or brass cages, and ISO P5/P4 precision grades, with 7000C/7200C series dominant in dryer and calendar rolls.

RV reducers in steel-mill auxiliary drives must be specified by torsional stiffness, thermal-rated output torque, backlash drift over 8,000 hours, and needle-bearing source rather than by brand. For hot-zone and high-thermal-capacity mill service, parallel-shaft and cycloidal reducer platforms rated
Retaining-ring selection in 2026 hinges on four gates: groove geometry (DIN 471/472 vs ANSI vs custom), material grade (AISI 1074/1095 carbon vs 302/316 stainless vs beryllium copper), load mode (radial vs axial, static vs rotating), and compliance (DIN, ANSI, JIS, GB). Bore/shaft diameter and rotat
Industrial sprocket total cost of ownership is dominated by downtime, lubrication, and tooth-wear-driven replacement, not the unit price on the PO. Lifecycle cost models in 2026 typically put purchase at 10-30% of 10-year spend, with energy, lubrication, and unscheduled stoppages carrying the balanc
A linear module is a complete ready-to-install linear-motion subsystem integrating a linear guide, drive element, bearing block and housing; a linear guide is the bare recirculating bearing rail. Choose modules for short stroke, low engineering effort; choose guides for long stroke, custom framing.

Steel mill linear actuators must be IP65+ electromechanical units, ball-screw or roller-screw driven, with 100% duty cycle ratings and load capacities up to 40,000 N, paired with absolute or incremental linear encoder feedback for slab shear, descaler and coiler position control. Hydraulic legacy sy

A fluid coupling sized on absorbed power and service factor, with working fluid matching ambient temperature and ATEX/IECEx zone, fits soft-start conveyor and crusher duty; for precision or reversing service a jaw coupling or disc coupling is the correct pick.

Shaft coupling selection in mining hinges on matching torque rating, service factor, misalignment capacity, and environmental sealing to the specific machine, with drum gear and tire couplings favored for crushers and ball mills, and diaphragm (disc) couplings preferred for high-speed, maintenance-f

Silent chains, also called inverted-tooth chains under ANSI B29.2M-1982, are the go-to spec for automotive timing drives and body-shop conveyor transfer lines where low noise, high speed and multi-strand load capacity matter. The 2026 selection playbook: confirm pitch (9.52–50.8 mm), tooth profile,
Downhole and surface roller bearings for oil & gas are specified against API Spec 7-1/7-2, NACE MR0175, and AISI 52100/8620 case-hardened steel, with API 6A PSL-3 gate-valve trim and ISO 15:2017 dimensional envelope governing the buy.
Pillow block bearing selection in 2026 is dominated by shaft-bore (e.g. 40 mm UCP308-25 at 220x60 mm, 2.2 kg), insert series (UCP205/UCP206 cast-steel 1.30 USD/set MOQ), housing material (cast iron, GCr15 chrome steel, stainless SI8T/K, polymer/igubal) and load regime — align to the four gates befor
Pneumatic conveyor selection hinges on four matched parameters: material bulk density, particle size, conveying distance, and phase mode (dilute, medium, dense). Powders with bulk density under 8 kg/L and particle size below 30 mm are ideal; otherwise dense-phase low-velocity plug flow is the safer

Steel-mill thrust bearing selection pivots on three gates: load type (pure axial vs combined), shaft speed (C0 static vs dynamic rating), and rolling-element family. For roughing-mill stand roll-balance cylinders and continuous-caster segment rollers, spherical roller thrust bearings dominate above

Angular contact ball bearings are specified for combined radial + axial loads where deep-groove ball bearings lack rigidity. Selection hinges on contact angle, duplex pairing, bore series, and limiting speed; 7019-series stock at ~1000 pc MOQ is widely quoted on B2B portals in 2026.
Pillow block bearing sizing starts from shaft diameter (12-140 mm metric bore) and load case, then maps to insert series (UC204-UC218, UCP/UCF/UCFL/UCT 200/300) and housing material (cast iron, pressed steel, stainless, polymer). Misalignment ≤2°, dynamic load up to 62 kN per typical UCFC/UCP 200-se
Crossed roller guide sizing is governed by four numbers — dynamic load rating C, equivalent load P, required travel life L, and the moment about the vertical axis — applied through the ISO 14728 bearing-life calculation family rather than a single rule of thumb.
Ceramic bearings (Si3N4 / ZrO2) run hotter, faster, drier and lighter than standard steel ball bearings but cost 5-10x more; steel ball bearings win on shock load, cost and chemical versatility. Hybrid and full-ceramic options split further on corrosion, electrical isolation and speed.

Ball bearing installation success depends on four control points: clean, dry, ambient-temperature mounting; shaft and housing tolerance matching to ISO metric fits; correct axial preload or radial play; and lubrication matched to speed and load. Use a ball bearing handbook for the matched bearing se
Match the belt tensioner to the belt type, load profile, and duty cycle: spring-loaded idler units for industrial blowers, automatic torsional-spring units for automotive accessory drives, and OE-part-numbered A/C tensioners for vehicle replacement. Verify pivot, bearing, seal, and spring service in
Slewing bearing FOB China prices in 2026 span roughly US$100/set for light flange units to US$900+ for triple-row roller pelletizer series, with single-row ball four-point-contact types clustering at US$450–500/piece on 1-piece MOQ.
Belt tensioners are classified by actuation principle (spring-automatic, hydraulic-damping, mechanical-adjustable) and by belt type (V-belt, multi-rib/serpentine, timing, flat). Matching the tensioner class to the v-belt, ribbed-belt, or timing-belt drive governs service life on automotive and indus

Timing pulleys are classified by tooth pitch (inch XL/L/H or metric T/AT/HTD), bore type (straight vs. taper), and belt series (MXL through S14M). Selection hinges on matching pulley pitch to the timing belt profile, OD/width envelope, and bore diameter for the shaft.

RV reducers deliver 5-10,000 Nm torque with single-stage ratios from 30:1 to 320:1 and backlash below 1 arc-minute, but cost 3-5x more than worm or helical alternatives and weigh noticeably more per kW of output. Best specified for six-axis robot joints, CNC rotary tables, and AGV drives where torsi
Pulp and paper mills run bearings through hot, wet, corrosive, contaminant-loaded service. Sealed deep-groove ball bearings with black-oxide or PTFE-coated rings and premium grease are the default for dryer, calender and roll-nip sections.

Tapered roller bearings remain the dominant radial-thrust solution for heavy mining equipment, sized by dynamic load rating C and bounded by the 1/10 (roller/race) conformity ratio. Match bearing series to contamination, impact load, and bore-diameter class before vendor selection.

Cement plants typically specify single-row TS, double-row TDO/TDI, or four-row tapered roller bearings depending on kiln, mill, and conveyor duty. Selection pivots on combined radial+axial load, RPM, contamination sealing, and clearance class rather than bore size alone.
For automotive production lines in 2026, tapered roller bearings are specified by load direction, bore range, and mounting style: NSK single-row units target transmission preload, while Timken TSRB (22.23–117.48 mm bore) and TSF (up to 1,270 mm bore) cover transaxles through machine-tool spindles. S

Self-aligning bearings in automotive production are spec'd primarily as double-row ball or spherical roller units with bores 10-160 mm, chosen to absorb shaft deflection and misalignment in transmission, gearbox, and conveyor drives. Selection hinges on load type, misalignment angle, lubrication reg

Pillow block bearing selection in mining hinges on four spec levers: housing material, sealing system, insert type, and bore size, mapped to shock load, contamination and wash-down exposure. NSK Life-Lube PBT housings cover 20-40 mm bores with Molded-Oil inserts for corrosive wash zones. For he
Industrial gears span spur, helical, bevel, worm, planetary, and cycloidal types, with selection driven by torque, ratio, efficiency, and duty cycle across petrochemical, mining, and OEM applications.

For 2026 agricultural machinery builds, taper bush selection starts with shaft diameter and bore series (1008 through 5050), then matches the Taper Lock / QD / Double Split Taper family to torque, environment, and maintenance access. Cast iron suits dry field duty; stainless or zinc-plated steel is

Universal joint selection for cement plants hinges on matching alloy U-joint or double-joint type to torque, angular misalignment, abrasive dust ingress, and impact load, with proper material and seal choice preventing premature cross and needle bearing failure in kiln, cooler, and raw mill drivetra

Universal joint selection for mining hinges on three measurable variables: transmitted torque, operating angle, and rotational speed. Single joints cap at 45° angular misalignment with non-uniform output velocity; double joints and CV assemblies reach 90° with constant-velocity output, the configura

For agricultural machinery, flange lock nuts and all-metal prevailing-torque nuts (DIN 980 / ISO 7042) outperform nylon-insert nylocks in high-vibration, high-temperature joints. Match the locking principle to vibration severity, temperature, and reuse, not to thread size alone.

Gear couplings dominate pulp and paper mill drivelines because they tolerate the high-torque, misalignment-heavy loads seen on refiners, calendars, dryer sections, and paper-machine drive shafts, with standard bores up to 5-3/8" and torque ratings to 220,000 in-lbs. Selection is a service-factor pro

Frictional locking assemblies transmit torque via 360° shaft-hub contact and are the dominant keyed-connection replacement for bulk material handling. Selection is governed by torque, bending moment, bore tolerance, and hub yield strength, not by shaft diameter alone.

For agricultural machinery, gear couplings are specified when drives must transmit high torque, tolerate shaft misalignment, and survive dust, shock, and moisture. Selection follows a torque-first method, with size and service factor driven by horsepower, RPM, load type, and starting frequency.

Marine gear couplings are sized first by continuous torque (lb-ft), then by misalignment envelope, with stainless or coated hubs specified for saltwater service. For engines above roughly 60 lb-ft, double-engagement gear couplings dominate propulsion lines; below that, elastomeric units handle vibra

Agricultural PTO drivelines rely on cross-type universal joints sized to the implement series (1-8) and ASAE PTO categories, with phased pairs and CV heads specified when operating angles exceed 25 degrees.

Food processing plant engineers should default to elastomeric or disc couplings for washdown zones and reserve gear couplings for high-torque sugar-mill or crusher drives, with material-grade selection, FDA-compliant elastomers, and balanced selection criteria driving every specification.

Fluid couplings are widely specified for textile-mill drives, with soft-start, overload protection, and shock-load damping reducing gearbox wear on carding, spinning, weaving, and dryer lines. Selection hinges on service factor, slip characteristics, fill ratio, and thermal rating rather than catalo

Steel-mill gear couplings are selected against shock, not nominal motor torque: hot-strip roughing and blooming mill spindles typically exceed 100,000 N·m, and the GIICL, NGCL, and WGT drum series cover most mill-stand, crane, and runout-table drives with two-year reconditioning campaigns as the rea

Spring washer selection for cement plants hinges on matching DIN 2093 disc springs, 17-7 PH or Inconel materials, and stack configuration to the 150-300°C kiln, cooler, and mill bolting. Belleville sets dominate high-preload joints, wave washers fit tight radial housings, and split lock washers rema

Pulp and paper mill belt drives demand tensioners rated for steam, moisture, and chemical exposure, with spring- or hydraulic-loaded automatic units favored over fixed-idler designs on critical lines. Selection hinges on drive layout, belt type, and ambient contamination.

For cement-plant drives, gear couplings are selected on five binding inputs: peak torque with a 1.5 to 3.0 service factor, angular/axial misalignment, bore size, ambient contamination, and lubricant sealing, with crowned-tooth hubs and flanged sleeves being the dominant constructions.

Steel-mill shaft collars are selected by matching set-screw vs clamp-style holding, steel grade, and finish to roll, reheat-furnace, and coiler duty cycles. Carbon and stainless dominate; clamping collars hold roughly twice the axial load of set-screw equivalents on hard mill shafts.

Mining-duty gear couplings transmit high torque between motors, gearboxes, mills, and conveyors under severe shock, dust, and heat, and are typically selected with a service factor of 1.75 to 2.5 per AGMA, angular misalignment held below 0.25 degrees, and relubrication every 2000 to 3000 hours. They

For packaging lines, select timing pulleys by matching pitch (HTD 3/5 mm or GT2 3/5 mm), tooth count, width, and food-grade material to the conveyor's torque, speed, and washdown class. The wrong pitch or too few teeth in mesh cuts belt life from 3,000 hours to a fraction of that.

Textile-mill drives should use ANSI B29.1 sprockets with no fewer than 17 teeth, hub style B or C, and 1045/4140 carbon or alloy steel heat-treated to 38-45 HRC, paired to a chain with a 3-4% speed reduction below driver RPM for stable fiber tension.

Jaw couplings sized for textile-mill drives typically land in the L, AL, or C series range, with spider material (NBR, Urethane, Hytrel, or bronze) chosen to match lint, humidity, and start-stop duty. Lovejoy's L line covers up to 12,500 in-lbs (1,412 Nm); the C line extends to 37,800 in-lbs (4,271

Jaw couplings with NBR SOX or Hytrel spiders cover 3.5 to 170,004 in-lb torque and 0.125 to 7 inch bores, suiting most automotive line drives when matched to motor kW, service factor, and misalignment budget.

Spring washer selection for material handling hinges on matching washer type (Belleville, wave, curved, split lock) to load profile, deflection range, and material, with Belleville disc springs for high-load joints and wave/curved washers for lighter vibration duty. Carbon steel, stainless steel (30

Jaw couplings are commonly specified for pulp and paper auxiliaries such as pump, fan, refiner, and calender drives where moderate torque, misalignment tolerance, and no lubrication are the deciding factors. Selection hinges on service factor, spider material, bore range, and ambient conditions, wit

For packaging lines, taper bush selection centres on a 1008-5050 size series with bore range 1/2-5 in, wrench torque 55-3,100 in-lbs, and torque capacity up to 126,000 in-lbs, matching drive load to bushing number and shaft tolerance.

Marine-grade lock nut selection hinges on matching four variables: substrate material (316 stainless, silicon bronze, aluminum, hot-dip galvanized steel), locking mechanism (nylon insert, all-metal prevailing torque, serrated flange, free-spinning structural), thread fit (jam nut pairs, prevailing-t

Gear couplings fit high-torque, low-speed packaging drive stages like conveyors, palletisers, and cap/sleeve applicators, but they need lubrication and are not the best pick for high-speed filling or labelling axes.

For marine service, jaw couplings should be selected as L, AL, or SS type with NBR or Hytrel spiders, rated for continuous torque with a 1.5–3.0 service factor, 316 stainless or aluminum hubs for salt-air exposure, and verified RPM under the 1,750 SW or 3,600 LC limit.

Jaw couplings specified for wind turbine drivetrains typically transmit 170-525 Nm via aluminum or stainless hubs with NBR or Hytrel spiders, with bore sizes 0.125-7 in and RPM limits 1,750-3,600. Selection requires shaft misalignment budget, spider durometer, and fail-safe validation, not generic c

Conveyor chain selection hinges on matching pitch, roller diameter, inner width, tensile strength, and material to load, speed, and environment. Stainless steel or polymer chains suit washdown and food lines, while carbon or hardened alloy steel is specified for bulk, mining, and high-temperature du

For material handling drives, jaw couplings are typically sized using service-factored torque, shaft bore, RPM, and misalignment limits, with elastomer spider choice driving temperature, damping, and replacement interval. Standard L/AL/SS hubs from Lovejoy span 3.5 to 170,004 in-lbs across 24 sizes

For packaging lines, choose conveyor chain by four filters: product (weight, footprint, fragility), downstream demand (flow vs accumulation), environment (washdown, cold, dry), and total lifecycle cost. Roller, double-pitch, stainless, and engineering attachment chains cover 90%+ of pack-line convey

For packaging-line drives, the default jaw coupling (L-type steel hubs, NBR spider) is the cost-effective choice at continuous torque below 1,412 Nm and bore up to 73 mm, while servo-indexed or registration-critical stages need precision zero-backlash designs with machined hubs and clamping hubs for

Hydraulic industrial shock absorbers sized for steel mill rolling stands, coil handling, and crane buffers convert kinetic energy to heat; selection hinges on per-cycle energy, cyclic rate, propelling force, and ambient heat dissipation, with a 30% safety factor above 240 cycles/hour and an 85% effi

Jaw couplings suit cement-plant auxiliary drives where moderate torque, misalignment tolerance, and zero lubrication are priorities, while mills, kilns, and crushers usually need gear or grid couplings. Selection hinges on service factor, spider shore hardness, bore fit, and ATEX/IECEx zoning around

V-ribbed belts (PK/Poly-V) are the preferred compact drive for pulp and paper machinery, selected by section (PH, PJ, PK, PL, PM), rib count, and length, and governed dimensionally by SAE J1459.

Jaw couplings are commonly selected for mining duty when torque is moderate, vibration damping matters, and lubrication is impractical, with bore sizes reaching 45 mm and rated torques of roughly 300 Nm (2,655 in-lbs) in large-frame designs. For higher continuous torque or shock loads, gear or

Disc couplings are the default shaft coupling for textile mill drive trains where misalignment, lint ingress, and continuous duty collide: lubrication-free AISI-301 disc packs, 1.05.0 service factors, and ATEX/API-610 rated packages sized at 1,7503,600 rpm.

For agricultural machinery drives, jaw couplings are typically the lowest-cost three-piece flexible coupling option when the duty cycle stays under about 12,500 in-lbs (1,412 Nm) and ambient exposure includes oil, dust, and moisture. Pick hub material by corrosion exposure, spider durometer by torqu

Disc coupling selection for automotive production is driven by torque density, misalignment budget, and EV drivetrain requirements; global demand reached USD 1.5 billion in 2025 and is forecast to grow at 4.96% CAGR through 2035.

V-belt selection for automotive production lines is governed by five verifiable inputs: drive horsepower, RPM, center distance, service factor (1.0 to 1.8), and classical or narrow cross-section (A/B/C/D/E or 3V/5V/8V). Matching these against cogged or wrapped construction prevents slippage, prematu

Wind-power sprocket selection runs on a 7:1 ratio ceiling, ANSI Type A/B/C/D hub rules, and high-strength alloy or carbon steel. Pitch, tooth count, bore, and chain standard govern fit and life.

Disc couplings are the dominant drop-in replacement for lubricated gear couplings on pulp and paper machinery, with torque capacity to 3,309,000 in-lbs, bore range to 10.5 in, and compliance to API 610/671.

For material-handling drivetrains, gear couplings remain the high-torque default when torque density, shock tolerance, and misalignment absorption all matter, sized by T = 9550P/n plus a service factor, not by motor nameplate alone. Use grid, elastomeric, or disc couplings when misalignment, electri

For agricultural machinery, select a disc coupling rated for at least 1.5x the driver service torque, AISI-301 stainless disc packs, ATEX certification if grain dust is present, and a configuration that handles the parallel, angular, and axial misalignment typical of tractor PTOs and mounted impleme

Constant-fill fluid couplings in the 300 W to 6 MW power range are the standard soft-start and torque-limit device for mining conveyors, with ISO VG 32 mineral oil typical, and water or HFD-U fluids required in hazardous zones. Selection hinges on load type, motor power, ambient temperature, and ATE

Steel-mill taper bush selection in 2026 is a material-and-load decision, not a brand decision: grade-25/35 cast iron, ductile steel, or stainless steel bushings are matched to shaft size, torque, and corrosion exposure. For hot-mill, pickle-line, and marine-coastal service, stainless or weld-on hubs

For material handling drives, disc couplings in the SU, SX, DI and SXC families from Lovejoy (a Timken company) are typically the go-to: zero-lubrication, all-metal disc packs in AISI-301 stainless steel, ATEX certified, and API-610 supported up to 3,800 RPM. Spec the coupling by design torque, then

For food processing, specify a 300-series stainless disc coupling with single-disc packs, food-grade lubrication-free hubs, IP66/IP69K seals, and a torque service factor of 1.5 or higher over the motor nameplate, validated against 3-A Sanitary Standards and EHEDG cleanability guidance for washdown z

Food-grade belt tensioners for processing lines must combine FDA 21 CFR-compliant contact materials, USDA-zone hygiene geometry, and tension control matched to PU or silicone belt elongation, with spring- or pneumatic-loaded automatic units preferred over manual slide adjusters on washdown drives.

For steel mill main drives (rolling mills, coiler/ decoiler, screwdown, runout table), disc couplings are commonly specified as double-flex units sized with a 1.5 to 2.0 service factor on the nameplate torque, with API-671 balance on turbines, API-610 on pumps, and ATEX on hazardous-area drives, whi

For cement plant drives above 75 kW running through dusty gearboxes, disc couplings with stainless disc packs, ATEX certification, and API-610 anti-flail compliance are the defensible 2026 default. Selection turns on torque, misalignment budget, ATEX zone, and inspectability, not catalog price.

Disc couplings are specified for high-speed mining drives where zero backlash, no lubrication, and ATEX certification matter; for heavy-load low-speed equipment like mills and crushers, gear or drum gear couplings remain the default. Selection pivots on torque, misalignment, speed, and dust/moisture

Clutch and brake selection for textile mills centers on matching torque, thermal horsepower, and inertia to each machine's duty cycle. Magnetic powder, electromagnetic, and oil-shear units each cover distinct spindle, winder, and baler duty profiles.

Silent (inverted-tooth) chain is the right pick for pulp-and-paper drives when high speed, low noise and long centre distances meet a corrosive, lint-laden environment. Specs to lock first: pitch series (3/16" to 1" and metric), hardened alloy-steel link plates, design horsepower with a 1.4-2.0 serv

Automotive production lines select clutches and brakes by matching actuation type (pneumatic, electric, hydraulic) to thermal capacity, static and dynamic torque, and cycle rate. Engineers first decide clutch-only, brake-only, or combined unit, then size against inertia reflected back to the shaft.

Marine timing pulley selection hinges on three gates: minimum 6 belt teeth in mesh, 316 stainless or hard-anodized aluminum for salt exposure, and IP67-sealed bearings. HTD 5 mm or 8 mm curvilinear profiles out-carry trapezoidal XL/L by 20-40% at equal pitch.

Pulp and paper mills specify clutches and brakes by station function: tension brakes (water-cooled, constant-slip) on unwinds, drum/shoe brakes on winder cores, and engine clutches on chippers. Selection pivots on thermal capacity, slip duty cycle, and torque density.

For packaging-line drives, a disc coupling is the go-to all-metal flexible coupling when zero backlash, lubrication-free operation, and 1/2° to 1-1/2° angular misalignment capacity are required. Selection hinges on torque density, disc-pack bolt count, spacer style, and ATEX/API-610 compliance.

Wind turbine brake and clutch selection is dominated by three functions: rotor (high-speed shaft) braking, yaw drive braking, and drivetrain over-speed protection. Hydraulic caliper disc brakes and spring-applied, hydraulically-released safety brakes are the two workhorse technologies for utility-sc

Stainless-steel or aluminum jaw couplings with food-grade elastomer spiders are the default spec for washdown food lines, sized to torque, bore, and IP69K cleaning exposure. Lovejoy spans 3.5–170,004 in-lbs across 24 sizes; Ruland offers food-rated versions up to 2,655 in-lbs (300 Nm).

Clutch and brake selection for material handling hinges on matching torque capacity, response time, and inertial load to a defined function, with electromagnetic, hydraulic, pneumatic, and mechanical-friction families each covering a different duty envelope.

Packaging-line clutches and brakes are sized by torque, cycle rate, motor frame, and hazardous-area class. For 0.5-1,250 lb-ft loads on NEMA 56C-440TC frames, spring-set power-off electric brakes remain the default; oil-shear and Division 1/2 hazardous-location units cover washdown and solvent envir

For pulp and paper mill drives, parallel rectangular keys (per ISO 773 / ISO 2491) sized to the shaft diameter and loaded to 50% of the shaft material's yield strength remain the default sunk-key choice; Woodruff keys are limited to small shafts, taper keys to low-speed heavy-torque joints, and feat

Food-grade clutch and brake selection hinges on three load-environment axes: motor horsepower, cycle rate, and corrosion resistance against caustic washdown. Oil-immersed oil-shear units with USDA H-2 fluid and nickel-plated or epoxy-coated housings dominate washdown-duty food lines, per OEM documen

For cement plants, two-piece split clamp-type stainless or zinc-plated steel shaft collars (1/2" to 3" bore) handle kiln, ball-mill, and conveyor service reliably. Avoid set-screw collars on case-hardened or chrome-plated shafts. Match material to dust, moisture, and temperature zones per process ar

Clutch and brake selection for steel mills hinges on dynamic torque at slip speed, heat dissipation, mill-specific duty cycle, and mounting interface. Spec sheets list MAX TORQUE (Nm), SLIP SPEED (rpm), and KINETIC POWER (W) as the three governing numbers for sizing any mill stand or coiler.

Pneumatic clutch-brakes up to 150,000 Nm dominate heavy-duty cement drive selection; air-actuated units with 1,225 hphr facing life and 80 psi max supply are the cement-plant benchmark.

For mining equipment, select clutches and brakes by matching duty cycle, torque capacity, and hazardous-location certification (MSHA, NEC Class I/II Div 1 or 2) to the host machine; oil-shear wet disc, spring-set pneumatic, and hydraulic-actuated units dominate shovels, mills, and conveyors.

Flexible elastomeric and gear couplings dominate textile-mill drivelines, with jaw, Oldham, and fluid couplings selected for specific misalignment, soft-start, or precision needs. Match torque (with service factor), RPM, misalignment type, and environment before vendor.

Cement-plant conveyor chain selection is governed by four stressors: abrasion from clinker/limestone, temperatures above 800°C at the kiln inlet, shock loading from chunk feed, and dust-driven corrosion. Match chain type (roller, apron/pan, drag, bucket-elevator) to the conveyor function, not to a g

Flat belt selection for automotive production hinges on four specs: belt material (polyurethane, nylon-rubber, fiber-reinforced), tensile cord, surface coefficient of friction, and pulley compatibility. Match these against line speed, load profile, and ambient temperature rather than choosing by pri

For pulp and paper mills, flexible couplings (gear, disc, grid, elastomeric, and fluid) dominate because they tolerate misalignment, shock, and corrosive, high-humidity service, while rigid couplings are reserved for precision-aligned sections like calendar stacks. Selection hinges on torque, servic

Disc couplings are the default all-metal flexible coupling for marine pumps, compressors and auxiliary drivesets where zero lubrication, API-610 balance and torsionally rigid response are specified. Marine-grade selections pair AISI-301 stainless disc packs with 4/6/8-bolt unitized designs, ATEX cer

Spring washer selection for textile mills centres on DIN 2093 disc springs in 17-7 PH or 301 stainless, with bolt-matched inner diameter (M6=6mm, M8=8mm, M12=12mm) and surface phosphate or zinc finish for high-speed assembly. Belleville wave or curved types solve loosening on looms, while POM plasti

Marine shaft couplings link gearbox output to propeller shaft and must handle saltwater, vibration, and thrust loads. Flexible elastomeric and rigid ductile-iron flange types dominate inboard drivelines, with selection driven by SAE J755 flange geometry, torque service factor, and misalignment toler

Agricultural drivelines on tractors, PTO shafts, balers, and mowers demand flexible couplings rated for shock, dust, moisture, and misalignment up to 4 degrees angular, with service factors of 2.0 to 3.0 applied to design torque. Selection centers on jaw, gear, disc, chain, and elastomeric types mat

Universal joints for textile mills should be selected on torque, continuous operating angle, rpm, and ambient lint/humidity. For most carding, spinning, and weaving drives, needle-bearing double Cardan joints in the 1310/1330/1350/1410 size family, in heat-treated alloy steel with sealed boots, are

For textile mills, the default Taper Lock series 1210-3525 in steel or ductile iron covers 70 percent of carding, draw-frame, and loom drives on metric shafts. Choose cast iron for low-speed dry sections, steel for high-RPM humid zones, and verify BS 4235 Part 2 conformity before ordering.

For packaging lines, jaw, disc, and elastomer-spider couplings handle 0.4 mm parallel and 1 deg angular misalignment while transmitting torque from servo motor to filler or labeler. Selection pivots on torque with service factor, bore H7/h6, DBSE, speed, and washdown material.

Specifying shaft couplings for food processing lines requires 304/316 stainless hardware, polished or encapsulated elastomer elements, and IP69K washdown capability, with flexible elastomer or disc types preferred over rigid or lubricated gear designs.

Steel-mill coupling selection hinges on matching torque, misalignment, speed, and thermal growth to one of four families: gear, disc/diaphragm, metal-bellows, or elastomeric. For hot-mill stands and continuous casters, gear and disc couplings dominate above 10 kN·m; metal-bellows couplings fit compa

For cement plant drives, gear, grid, and disc pack couplings are the three workhorse families specified for crusher, kiln, and high-power conveyor service, with torque envelopes commonly spanning 3,900 Nm to 2,900,000 Nm. Selection is driven by torque plus service factor, angular and parallel misali

Gear couplings in wind turbines transmit torque between the rotor/gearbox and generator while compensating for misalignment, vibration, and shock loads. Selection is driven by torque rating, bore range, misalignment capacity, lube-free service, and electrical isolation to prevent bearing-damaging ed

Food-grade roller chain selection hinges on matching material, seal design, and lubrication to USDA/FDA zone requirements rather than catalog kW alone. Stainless 304/316, nickel-plated, or coated chains paired with food-grade lubricants dominate Zone 1/2 washdown applications. Temperature derating c

Linear modules built on ball-screw or belt drives are specified for textile-mill yarn feeding, weaving shuttles, knitting needles, and fabric inspection when repeatability and tension control matter. Selection hinges on load, stroke, speed, accuracy, environment, and duty cycle rather than catalog m

Linear module selection for automotive production lines hinges on four binding criteria: drive type (ball screw, belt, or linear motor), positioning accuracy class, dynamic load, and stroke length, matched to each station's duty cycle. Ball-screw modules dominate precision stations like welding-gun

For textile mill drives, gear couplings sized to rated torque, bore fit ≤0.1 mm, ±2° angular and 1.0–1.3 mm radial misalignment capacity, with continuous-sleeve or half-gear variants for ring spinning and looms, are the spec baseline. Match torque to kW/rpm curves, keep peak motor torque ≤2× couplin
For packaging lines running 0.37–250 kW motors at 720–3600 rpm, a constant-fill or variable-fill fluid coupling sized at 1.5–2× the motor nameplate kW with a soft-start delay of 3–8 seconds protects gearboxes from shock loads during startup, labeling, and capping stations. Stainless-steel (1.4404/31

Linear module selection for agriculture machinery hinges on seven application factors: load, orientation, speed, travel, precision, environment, and duty cycle. Match these against enclosed ball-rail versus roller-rail linear guides, IP65K-rated actuator housings, and stainless or coated screw drive

For automotive production lines, gear couplings are the right pick when torque density, angular misalignment tolerance (0.5°–1.5° per mesh, peaks to 6°), and high torsional stiffness matter; sizing follows a 1.5–2.0 service factor on calculated torque, a 1:1 hub-length-to-bore ratio, and AGMA 9000 s

Marine linear module selection starts with IP67/IK08 enclosure rating, 316L stainless or hard-anodized aluminum housing, and drive type matched to stroke, payload, and saltwater exposure. Belt, ball screw, and linear motor types each cover different marine duty cycles.

Electric linear modules and actuators for wind turbines must be selected by stroke length, thrust, environmental rating, and grid-side converter duty cycle; pitch, yaw, and brake-calliper functions each demand distinct force/position profiles.

Food-grade sprocket selection centers on four decision axes: material grade (304 vs 316 stainless, acetal, UHMW, aluminum 6061/7075), tooth count (17T minimum at high speed/load), hub type per ANSI A/B/C/D, and strand count. Match pitch to chain exactly; for washdown lines, 316 stainless or self-lub

Linear module selection for material handling hinges on five paired decisions: load + stroke, drive type, accuracy + repeatability, installation orientation, and environment. Ball-screw, timing-belt, rack-and-pinion, and linear-motor modules each map to a distinct payload/speed envelope, and mis-siz

Linear module selection for packaging lines hinges on matching drive type (belt, ball-screw, rack-and-pinion, linear motor) to cycle rate, stroke, and IP rating. IP65 stainless-steel carriages and sealed bearing blocks are now standard for washdown and pharmaceutical packaging cells, and stroke rang

Food-grade linear modules are specified by food zone, washdown chemistry, and surface finish rather than catalog stroke alone. IP65K or IP69K housings with stainless or coated steel, FDA/EHEDG-aligned materials, and belt or ball-screw drives matched to throughput are the core decision points for 202

Steel-mill linear modules need heavy-duty rack-and-pinion or ball-screw units in steel housings with IP54+ sealing, sized at 1.5–2x the running load to handle scale, heat, and continuous duty. Match drive type, stroke, and repeatability to the mill stand, not the clean-room playbook.

Steel-mill roller chain selection hinges on four checks: ANSI/ISO pitch matched to sprockets, design horsepower with a 1.0–1.7 service factor, hardened WH or through-hardened WR series for abrasive service, and wear-elongation limits near 1.5% for power drives.

Steel-mill belt drives above 75 kW typically pair a constant-force spring or hydraulic tensioner with a heavy-duty V-belt or synchronous belt, sized by drive power, speed, torque, and ambient steel-mill conditions per CEMA guidance.

Linear module selection in cement plants hinges on dust-sealed ball-screw or rack-and-pinion drives sized for abrasive, high-temperature service. Specifiers should match stroke length to installation clearance, apply 1.5 to 2x safety factors on dynamic load, and pick IP65+ housings for kiln and preh

Marine fluid couplings for ship drivetrains must be selected on four hard criteria: rated power match to propulsion auxiliaries, fill type (constant vs variable), slip under load, and built-in safety features such as release or percussion caps, with hydrodynamic units covering size 185 through size

Linear module selection for mining operations centers on matching heavy-duty payload, long stroke, IP65+ sealing, and dust-tolerant drive trains to harsh, high-vibration environments. Belt, ball-screw, and rack-and-pinion modules each serve distinct haulage, transfer, and positioning roles undergrou

Crossed roller guides suit textile-mill short-stroke axes where high stiffness, smooth motion, and resistance to lint contamination matter more than long travel. Selection hinges on load direction, cage style, sealing, and corrosion-resistant materials for humid cotton-yarn areas.

Wind turbine disc couplings are selected by torque rating, misalignment capacity, electrical isolation, and corrosion class; composite disc packs rated -57 to 121 C with C4 corrosion resistance dominate modern drivetrains. Single flex-plane, floating-shaft, and close-coupled architectures each

Crossed-roller guides suit pulp-and-paper mill duty when stroke stays under ~1 m, loads are high, and stick-slip-free motion matters. Selection hinges on cage material, sealing, lubrication, and corrosion-resistant materials, not catalog headline capacity.

Crossed roller guides suit agricultural machinery where short-stroke, high-shock, and high-contamination duty cycles dominate, with a typical selection limit under 1 m of travel. Spec load rating, preload class, sealing, and lubrication before matching a series to a tractor, sprayer, or harvester ax

Crossed roller guides are specified for marine equipment when stroke stays short, loads combine (radial + axial + moment), and corrosion-resistant housings or seals are required. Selection is governed by ISO dimension series, material grade, preload class, and sealing, with the marine envelope addin

For packaging lines, crossed roller guides are typically chosen over recirculating ball linear guides when stroke stays under ~200-300 mm, loads are predominantly vertical or moment-loaded, and straight-line accuracy must hold within 0.0001 in/in of travel on aluminum or 0.00008 in parallelism on st

Crossed roller guides are specified for food and beverage lines when compact load capacity, high rigidity, and corrosion-resistant construction outweigh travel-length limits, with stainless-steel linear guides and CRBs dominating washdown zones. Selection is driven by radial/axial/moment load envelo

Crossed roller guides are specified for steel mill service when stroke stays under 1 m, load is multi-directional, and rigidity matters more than speed. Selection hinges on load direction, moment, mounting class, and contamination control, not catalog part number.

Crossed roller guides fit cement plant service when stroke stays under roughly 1 m, abrasive dust is managed by sealing, and tilting moment plus radial load dominate. For dusty, heavy-vibration zones like clinker coolers and roller presses, specify sealed crossed-roller ways with preloaded cages, co

For textile mills, pick a ball spline by mapping the worst-case axial load, moment load, RPM, and travel life against the four-groove medium-torque or high-torque caged-ball type, then verify critical speed and lubrication duty. Four-groove gothic-arch contact typically delivers 5 to 12 times the lo

Ball spline selection for automotive production is governed by three THK-defined families: high-torque, medium-torque, and rotary types, sized on stroke, load, torque, and moment demands per ISO-style bearing-life equations. Linear variants held 58.3% of the 2025 USD 411M global market, with Asia Pa

Ball splines in pulp and paper mills serve three duty profiles: reel-spool anti-rotation, calender/slip torque transfer, and winder traverse under steam and washdown. Spec gates: shaft diameter 15–60 mm, contact angle 20° vs 45°, dynamic load 5–12x a slide bush, and four-groove gothic-arch geometry.

Ball spline selection for agriculture machinery hinges on matching shaft diameter, accuracy grade, and torque class to dusty, shock-loaded field duty. Solid 15–40 mm shafts in H or P grade with medium-torque LT/LF nuts dominate sprayer booms, planter rows, and combine headers, while high-torque LBS/

Ball splines for wind power yaw and pitch drives are selected around three hard constraints: high torque transfer under cantilever load, grease life at low RPM, and ISO 3408-class precision. A medium-preload (P1–P2) caged-ball spline on a through-hardened SUJ2 shaft, 55–60 HRC, is the default 2026 r

Ball splines for packaging lines should be specified as a stroke-limited rolling element with P0 zero preload for metering axes, P1 light preload for cantilever cross-seals, and 440C stainless on 440C stainless with food-grade lubricant for washdown. Shaft diameter 10.4 mm at 2400 N dynamic load cov

Food-grade ball splines in stainless 440C shafts, 55 HRC minimum, with food-grade H1 grease and IP66 sealing, are the working spec for washdown bottling, slicing, and pick-and-place lines in 2026.

For steel-mill service, specify high-torque 45° angular-contact ball splines on EN 1.3505 / SUJ2 shafts at 58 HRC, in 15–100 mm nominal diameters, with seal kits and continuous grease lubrication. Avoid medium-torque 20° contact types where roll-changing torque loads or mill scale contamination are

For cement plant duty, a cement-mill-proven ball spline spec stacks a 20-30 mm induction-hardened shaft (EN 1.3505 / 100Cr6 family, ≥58 HRC), a sealed caged-ball nut with negative preload, and an IP65 boot, with catalog torque ratings of 25-45 N·m static on a 20 mm unit and dynamic radial load held

Pulp and paper mills push lead screws through steam, stock chemicals, and abrasive fiber carryover, so selection hinges on material, lubrication, and envelope rather than load rating. Specify 300-series stainless or nickel-plated carbon steel with food-grade grease, expect 1.5-3 year service in drye

Marine lead screw selection hinges on three saltwater-specific decisions: 316L or super-duplex stainless versus bronze nuts, ACME 29° or trapezoidal 30° thread geometry matched to regional standards, and ISO 4413/2788 ingress protection over 150 RPM duty cycles. Trapezoidal threads in diameters from

Lead screws for material handling are specified by matching thread direction, thread size, and number of thread starts, with lead accuracy of 0.18 mm/300 mm and efficiencies of 35% to 85% across Acme, trapezoidal, and stainless variants. Selection hinges on load, speed, duty, corrosion, and backlash

Lead screws for packaging lines are sized by 5 spec gates: lead (mm per rev), dynamic thrust load, number of thread starts, duty cycle, and corrosion class. Match thread size, direction, fit, and starts on screw and nut to avoid binding or premature wear.

For food processing lines, lead screw selection hinges on stainless construction (typically 304/316), food-grade polymer or bronze nuts, trapezoidal threads for washdown compatibility, and lubricant-free operation to meet FDA and EU 1935/2004 hygiene requirements.

Lead screws in cement plants are sized to 16–63 mm nominal diameter, 5–20 mm lead, and 10–100 kN static load ratings per ISO 3408, with GCr15 shafts and grease lubrication. Use enclosed ball screws only where dust ingress can be excluded; otherwise specify ACME or stainless lead screws with dry-film

For mining-duty linear motion, lead screw selection hinges on three gates: dust/water sealing (IP65+), self-locking trapezoidal threads for vertical loads, and material hardness (SCM440/42CrMo) for abrasive environments. C3-C7 ISO 3408 accuracy and 16-80 mm diameter range govern the rest.

Electric linear actuators for textile mills must be specified by force (1,000–6,000 N typical), stroke, IP rating for lint/humidity, and duty cycle; 24 V DC brushless or 12 V DC units dominate loom and tenter frame retrofits.

Linear actuator selection for automotive production hinges on four spec gates: dynamic force, duty cycle, IP rating, and feedback type. Use a 50% force design margin, size stroke from retracted-to-extended travel, and pair rod actuators with ball-screw or roller-screw transmissions when cycle rates

Pulp-and-paper linear actuator selection hinges on three gates: IP65+ washdown enclosure with stainless or hard-chrome rails and H1 lubricant for fibre-laden zones, repeatability of ±0.01–0.05 mm matched to slitter/reel/calender/headbox duty, and force-model sizing that includes tension, umbilical d

For 2026 agricultural machinery, electric linear actuators are specified at 12/24 V DC with 2000–12000 N thrust, IP65–IP67 ingress protection, strokes of 50–600 mm, and a 10% duty cycle. Selection is driven by load class, IP rating, stroke length, and feedback options.

Linear actuator selection for material handling is driven by four binding inputs: peak/holding load, stroke, duty cycle, and IP rating, with 2026 OEM force bands spanning 50–15,000 N across micro, standard, heavy-duty, and tubular classes. IP65 is the de-facto industrial baseline, while 24V DC trape

Electric linear actuators sized for packaging lines need F design = (W·μ + F process)·SF, with 24 V DC rod styles common for 2-12 in changeover strokes, ball screws for precision, and pneumatics only for sub-0.2 s reject strokes. Selection pivots on force, stroke, IP rating, and feedback.

Food-grade linear actuators for processing lines should be specified to IP66 or IP67, use 304 or 316 stainless housings, and run on NSF-H1 food-grade lubricants, with stroke, force, and duty cycle matched to the valve or cutter task at hand.

Cement-plant linear actuators need IP65+ sealing, 6,000 N minimum thrust for damper and kiln-feed duties, 10-25% duty cycle rating, and DC 24V supply, with 304/316 stainless housings where raw-material dust contacts the rod.

For mining duty, electric linear actuators are typically specified from 3,500N up to 17,000N with IP65/IP66 sealing, 25% to 35% duty cycle, and -40°C to +65°C operating range. Lead-screw units suit high-thrust, low-cycle work, while ball-screw actuators handle higher duty and accuracy. IP69K and ful

Ball screws for automotive production must be selected against axial load, precision grade, DN speed, and cleanliness, with nominal 6-50 mm screws limited to 50 μm backlash and 85% minimum efficiency per Chinese automotive brake ball screw assembly standards.

Ball screw selection for agriculture machinery hinges on five interlocking parameters: dynamic load, lead, total length, accuracy grade (C7 for general farm equipment, C5 for precision planters), and dust/corrosion sealing. A typical seeder or sprayer lift axis needs 1.5-3.0 kN dynamic load at C7 ac

Ball screw selection for material handling hinges on four coupled parameters: dynamic axial load, critical speed, lead (mm/rev), and duty cycle. Use a dynamic-load safety factor of at least 3x the working load, then pick shaft diameter from a 12-50 mm range against stroke length. Match C7-C5 accurac

Mining-duty ball screws must be sized against four gates: axial load, critical speed, buckling/column load, and DN value, with sealing and lubrication sized for dust and pH 3 to 11 exposure. Ground, rolled, and thread-whirled variants from 6 mm to 80 mm shaft diameter cover most mining-actuator requ

Textile mills typically specify profile linear guides (RGW20, RGH-series, V-rail) with corrosion-resistant coatings, self-aligning rails, and sealed blocks to survive lint-laden, humid, and chemically aggressive zones across spinning, weaving, knitting, and finishing lines. Selection gates center on

For automotive production lines in 2026, a linear guide is selected against four gates: rail width matched to carriage load (typically 15–65 mm), rolling-element type, accuracy class (C5/C7 per JIS B 1192-1), and lubrication environment. Steel rails dominate engine and battery assembly, while crosse

Linear guide selection for agriculture machinery hinges on sealing class, contamination rating, static safety factor fS = C0 / P ≥ 2 to 5, and stainless or zinc-nickel options for spray and fertilizer exposure, per current vendor guidance.

For marine service, specify 316 or 316L austenitic stainless linear guides with sealed sliders, derate dynamic load by at least 25%, and match IP rating to splash zone. Ball vs roller choice is set by load, not environment.

Linear guide selection for material handling hinges on rated load, accuracy class, and environmental exposure; standard carbon-steel ball guides serve most conveyor and gantry duties, with stainless or miniature profiles reserved for washdown or compact assemblies.

For packaging line builders, HG-series 15-65 mm linear guides with ZA preload match HIWIN/THK footprints and survive 300 packs/min HFFS duty. EG-series low-profile rails suit VFFS jaws; MG miniature rails fit compact end-of-line modules. Specify by speed, load, and IP65 sealing, not brand alone.

Slewing drives are not standard textile equipment: a 2026 mill line is specified around helical, helical-bevel, worm, and planetary gear reducers, with slewing drives reserved only for cloth-pallet turntables and stenter-frame transfer tables that need 90-degree index motion, torque hold, and IP65 l

Slewing drives for automotive production cells should be selected on three independent load vectors (axial, radial, tilting moment) before any catalog step. Standard SE3-SE25 models cover 1-60 kN·m; helical-worm units beat worm-only builds by 30-50% continuous torque at the same OD.

Slewing drives for agriculture machinery should be selected by matching OD, output torque, and sealing class to the implement: medium 7-15 inch (180-380 mm) units delivering 8,000-50,000 Nm output torque dominate planters, grain carts, and irrigation booms, while small 3-7 inch (75-180 mm) sealed un

Marine slewing drive selection is dominated by corrosion resistance, seal integrity, and combined axial-radial-moment load capacity, typically in the 7-25 inch (180-700 mm) OD range. Output torque from 8,000 to 50,000+ Nm and IP65+ sealing are baseline for ship-to-shore and offshore crane duty.

Wind turbine slewing drive selection hinges on four engineering gates: wind-load capacity, low-speed architecture (typically 0.01–10 RPM), gear self-locking, and a 20-year bearing life. Double-row four-point contact ball slewing bearings in 42CrMo dominate pitch and yaw positions on utility-scale tu

Slewing drive selection for material handling hinges on five load-and-motion parameters: tilting moment up to 1,200 kNm, axial/radial load, output torque up to 450 kNm, gear ratio between 10:1 and 100:1, and IP class matched to dust or washdown exposure. Worm gear units dominate lifting and tilting

Specifying a slewing drive for a packaging line is a combined-load problem: axial load ratings up to 250 kN, radial loads to 120 kN, worm or planetary gearing on a slewing bearing, and IP69K sealing for washdown, sized using a 30 percent shock safety margin.

Slewing drives for food processing are typically specified in the 5 kN to 250 kN axial load band with IP65 to IP69K sealing, 316 stainless housings, and H1 food-grade lubricant; worm-geared units are preferred where self-locking is required, planetary units where efficiency above 90 percent is requi

Slewing drive selection for steel mills anchors on three numbers: service factor 2.0-2.5, output torque 18,000-35,000 Nm for screw-down duty, and IP65 minimum ingress protection, with FEM M5 or AGMA 2001 duty-class ratings applied to the rolling-mill duty cycle.

Cement-plant slewing drives are typically sized between 5 kN·m and 350 kN·m output torque at 1:30 to 1:180 ratio, with worm-gear single-axis units common for mixers and planetary dual-axis units specified on preheater and cooler turrets. Selection is driven by dust IP class, ambient temperature, til

For mining rigs in 2026, specify worm-gear slewing drives (self-locking above 30:1 ratio, IP66/IP67 sealed) on inclined drill masts, roof bolters, and crusher feed booms, and reserve planetary or hydraulic slewing drives for stacker-reclaimers and large 360° excavators that need continuous rotation.

Variable speed drives for textile mills are selected by matching speed range, torque profile, overload rating, and environmental sealing to the process: 1:10 to 1:100 induction-motor VFD control is common, with 150% overload for 60 s and IP54 panels typical for humid mills.

Variable speed drive selection for automotive plants hinges on matching kW, voltage class, enclosure IP rating, and torque profile to the specific workcell, with a body shop typically using 1.5–75 kW VFDs and test-cell regenerative drives above 500 kW. IEC 61800 series drives with built-in STO, Prof

Variable speed drive selection in pulp and paper mills hinges on matching torque profile, voltage class (400V/690V), and section duty to AC vector, DC, or servo topologies, with retrofit economics driven by 20–30% AC-vs-DC cost premium.

Variable speed drives (VSDs) dominate modern wind turbines, with 72 of 95 surveyed 1+ MW models using full variable-speed architectures versus only 9 fixed-speed units. Selection centres on generator type (DFIG, PMSG, WRSG), converter topology (full-converter vs partial-converter) and grid-code reac

Variable speed drive selection for conveyors and other material handling equipment starts with four hard numbers: motor kW, full-load current at the actual supply voltage, worst-case overload, and the shaft-speed envelope. Sizing on FLA not horsepower, applying a 150%/60s heavy-duty reserve, and mat

On a packaging line, a VFD earns its keep through speed matching, phase-locked synchronization, and recipe-based format changeover, not the 20-35% energy savings quoted for pumps. Realistic energy gain on a packaging machine is 5-15%, while the harder jobs are indexing control, registration between

Variable speed drive selection for food processing hinges on matching drive topology to load profile, motor class, and washdown ingress rating, with IE4/IE5 motors on VSDs delivering measurable conveyor and pump energy savings across continuous-duty lines.

For steel mills, select low-voltage VFDs with direct torque control or closed-loop vector control, inverter-duty motor insulation, and active front-end harmonics on any drive above 100 hp to handle rolling-mill shock loads.

Variable speed drive selection for cement plants hinges on four live motors: kiln main drive (3-5x starting torque, 0.5-5 rpm), raw mill and cement mill (constant torque), and ID/FD fans (quadratic torque). Modern IE4/IE5 motors paired with regenerative VFDs can deliver 15-25% energy savings and 40%

Variable speed drives for mining cover low-voltage fans (under 250 kW) through 2.3-13.8 kV hoists and mills (400 kW to 25+ MW). Selection pivots on motor voltage, current and overload duty, with hazardous-area and IP rating constraints applied last.

Textile-mill helical gear reducers in 2026 cover 0.12 kW to 200 kW with 5:1 to 100:1 ratios, ISO 6 gearing, 60 to 78 dB noise, and IP54 to IP65 sealing. Spinning favors parallel-shaft helical; winders and small looms favor right-angle helical-bevel or worm units at 60 dB. Match the family to the mac

Helical gear reducers dominate continuous-duty paper machine sections at 96-98% per-stage efficiency, while right-angle helical-bevel units handle refiner and pulper shafts needing 1.25-450:1 ratios and up to 900,000 N.m output torque.

Helical-worm reducers sized SS37-SS97 (0.12-22 kW, 6.8-286.4 ratio, 90-4000 Nm, HRC58-62 gears) and inline helical R-series (0.12-160 kW, 94-98% efficiency) are the two spec families most commonly shortlisted for tractor, mixer, conveyor, and PTO-driven farm equipment. Selection hinges on duty cycle

Helical gear reducers for material-handling conveyors should be selected on four inputs: AGMA 6034 service factor, ratio+stage count, shaft-orientation family, and thermal-plus-overhung load verification. The decision rule: specify helical inline (R/MD) 5:1 to 300:1 for horizontal belts, parallel-sh

For food processing lines, specify helical gear reducers with 316L or 17-4 PH stainless housings, IP69K sealing, EPDM shaft seals, and 96-98% per-stage efficiency above 3 kW; verified 2026 supplier data shows F-series units from 0.18-260 kW and ratios 3.77-276.77 are the workhorse range for conveyor

For steel mill service, helical gear reducers in the F/MJ/K series cover 0.18–220 kW, 3.81:1 to 281.71:1 ratios, with parallel or bevel-helical layouts, 94–96% efficiency per stage, and ground 20CrMnTi gears at HRC 58–62 for hot, shock-loaded duty.

Helical gear reducers in the 0.18–22 kW range with 90 to 4,000 Nm output torque dominate cement plant auxiliary drives, while 1–6 MW integrated bevel-planetary units handle vertical roller mills. Select by duty class, ratio band, thermal capacity, and dust-sealed housing, not by horsepower alone.

RV reducers in the RV30/RV40 size range are the practical default for textile-mill gearing where noise must stay at or below 65 dB, vibration protection of yarn matters, and 24/7 weaving/knitting duty cycles apply. Selection hinges on center distance, reduction ratio, backlash, and ingress rating, w

RV reducers specified for marine service must pair ≥2500 N·m torque with CCS or DNV type approval, hardened bevel gearing at HRC 60, and a 4-stage housing rated for 95%–96% efficiency under cyclic rudder loads.

RV reducers for packaging lines are specified across ratios of 5:1–60:1, output torque of 10–1,200 Nm, and torsional rigidity of 372–7,448 Nm/arc.min., with backlash at 0.5–1 arc.min. Selection hinges on service factor 1.5–1.75, IP65/66 sealing, and IEC 60072 input flange for line integration.

RV reducers for food processing need 304/316 stainless or coated housings, NSF H1 lubricant, FKM double-lip seals, and IP66 sealing, paired with ratios from 15:1 to 100:1 and service factors 1.25–1.75. Cycloidal-pin geometry survives shock loads 3–5× nominal during conveyor jams.

RV reducers for cement plants are selected by output torque band, ratio range, mounting geometry, dust sealing, and continuous-duty thermal rating. Cycloidal RV-EM units span 98–4900 Nm at ratios of 27–37.34, while bevel-helical DBY/DCY units cover 8–50 ratios at 160–800 mm center distance for 24/7

Harmonic-drive reducers in automotive production fit robot-joint and AGV steering axes where 50:1 to 120:1 single-stage ratio and ≤60 arc-second transmission error matter more than raw torque. For continuous torque above 500 Nm, shock-loaded transfer lines, or paint-shop rotary indexing, planetary o

Pulp and paper winding duty imposes steady low-speed torque, moisture, and 24/7 cycling that push harmonic reducer selection toward mid-frame units (frame 14-20) with 50:1-120:1 ratios, ≤20 arc-sec backlash, and grease-lubricated 5,000-15,000 hr life ratings.

Harmonic-drive (strain-wave) gearheads sized for marine duty typically run single-stage ratios of 50:1 to 120:1, transmission errors of 60 to 90 arc-seconds, and rated output torques of 7 to 1,236 N·m in a 2.5 kg coaxial package, with 316L housings and IP66 sealing the two non-negotiable marine delt

For wind power yaw and pitch drives, harmonic reducers with single-stage ratios of 50:1 to 120:1, ≤60 arc-second transmission error, and rated torque from 3.7 to 67 N·m are the spec sweet spot. Cup-style units (DHS-25-100-U class) fit nacelle yaw axes; hat-style (DHDG-14-50-U class) suits short-axia

Harmonic-drive reducers win material-handling and robot-joint specs where sub-arc-minute repeatability and a 30:1 to 160:1 single-stage ratio matter, but the flexspline's shock tolerance caps at roughly 1.5x to 2x rated torque, so cycloidal or RV stages still own heavy shock-load duty cycles.

Harmonic drive reducers sized for packaging lines should be picked on full torque-speed cycle, lost motion, and torsional stiffness, not on ratio alone. Cup-type for shoulder/base axes carrying tilting loads, hat-type for hollow-shaft wrist and delta pick-and-place; backlash targets sit at ≤10 arc-s
For food processing, specify a cup-type or hat-type harmonic reducer with food-grade H1 lubricant, 300-series stainless external hardware, IP65 sealing, and a service life of 20,000–30,000 h under washdown conditions. Match the reducer's backlash class (typically under 1 arc-min) and ratio range (30

Harmonic drive reducers deliver 30:1-320:1 single-stage reduction with near-zero backlash, but steel-mill duty exposes them to vibration, heat, and shock that demand careful sizing. Plate-type designs now cover the 10:1-30:1 gap that cup-type units cannot.

Harmonic drive reducers are not the right pick for cement-plant main drives: zero-backlash strain-wave units belong in robotic joints and aerospace, not in 100-meter rotary kilns running 0.5–5 rpm. Specify K Series helical-bevel or RV reducers with 95–97% stage efficiency and IE5 motors instead.

Harmonic-drive reducers are entering mining duty cycles via quadruped inspection robots and autonomous equipment joints, with single-stage ratios of 30:1 to 320:1 and standard catalogue frame sizes from 8 mm to 350 mm diameter. For typical underground and surface mining, specify continuous torque wi

Cycloidal reducers with single-stage ratios up to 119:1 and torque ratings commonly sized 4.6-154 kg suit textile mill drives, but their higher noise and lubrication demand rule them out for cleanroom-style spinning rooms. Selection hinges on ratio, duty cycle, and ambient lint load.

For automotive production, a single-stage cycloidal reducer with a 5:1 to 100:1 ratio, ±0.005 mm eccentric tolerance, and 500% shock-load tolerance is the standard match for conveyors, palletisers, and welding-positioner drives. Specify a cycloidal unit when shock, reverse-duty cycling, and zero-bac

Cycloidal reducers running 85 to 95 percent efficiency are specified for pulp and paper mills when shock overload tolerance and right-angle mounting matter more than top-end efficiency. Selection pivots on service factor, moisture/steam exposure, and verified shock capacity.

For utility-scale wind turbine drivetrains, a cycloidal (cyclo) gearbox is the right call when shock tolerance, single-stage ratios above 50:1, and compact nacelle packaging outweigh the higher unit cost. Spec it on service factor 1.5+ for yaw and pitch duty, and 2.0+ for main rotor duty.

Cycloidal reducers deliver 85 to 95 percent single-stage efficiency with high shock tolerance, fitting packaging lines, indexing drives, and robot actuators. Selection hinges on ratio frame size, service factor, mounting, and lubrication match.
Cycloidal reducers fit food processing mixers and start-stop conveyors that need high reduction ratios and shock-load tolerance, with 85-95% efficiency; specify them only when hygiene, mounting, and duty cycle match. Use K-series helical-bevel or R/F-series units where washdown, low ratio, or tight

For steel mill drives, size a cycloidal reducer for hot-side shock loads first, verify 2-3x torque margin over flex spline equivalents, and confirm service factor for 24/7 rolling mill duty. Planocentric units out-torque harmonic drives of similar size and tolerate the impact events that kill thin-w

For cement plants, the cycloidal reducer is best specified for agitators, mixers, and bucket elevators where shock loads dominate, not for the rotary kiln main drive itself, which still calls for a hardened helical or cylindrical gear unit.

Cycloidal reducers run at 85 to 95% efficiency and dominate heavy-shock mining duties because multi-pin rolling contact splits the load across many contact points, but the right size for a crusher, conveyor, or hoist drive still comes down to service factor, ambient dust, and starts-per-hour, not mo

Marine gearbox selection hinges on matching gear geometry to shaft layout, with helical gears dominating modern propulsion at 98-99% efficiency and 50% higher load capacity than spur equivalents. Copper-alloy and case-hardened steel units suit saltwater service when paired with oil coolers sized to

Wind turbine gearboxes in 2026 are sized for ~3-7 MW onshore units and 8-15+ MW offshore, with planetary + helical stages dominant. Selection hinges on torque density, FZG stage ≥12 oil, and 20-year service life, per OEM data.

Industrial gear selection for material handling rests on matching gear type to shaft arrangement, service factor, and load pattern. Spur, helical, bevel, worm, and rack-and-pinion each map to specific conveyor, hoist, and AGV duties, with service factors of 1.25-2.5 governing gearbox sizing.

Helical, planetary, and spur gear drives each fit a different slot on a packaging line: helical gearmotors (0.18-2.2 kW, 10-300 rpm) for conveyors and fillers, planetary and harmonic units for indexing and palletizing, spur gears for low-cost torque transfer. Selection is governed by output speed, t

For food processing lines, helical, bevel-helical, worm, and stainless washdown gearboxes dominate selections, with food-grade H1 lubrication and IP66+ sealed housings as the hard filter; spur gears fit auxiliary dry zones where SUS303 or SUS316 stainless is specified.

Steel mill gearboxes must be sized for AGMA service class III (2.0 or higher), IP65 sealing minimum, and ambient temperatures of 60-80 C near rolling lines. Planetary and bevel-helical units dominate rolling-mill and cooling-bed drives above 3,000 hp input.

Cement plant gearbox selection is application-driven: planetary units dominate high-torque grinding mills, helical and DBY/DCY bevel-helical units cover 24/7 belt conveyors, and kiln drives rely on open girth-gear systems. A 4,500 TPD raw mill gearbox failure in 2026 cost $1.2M, framing why monitori

Mining gearbox selection hinges on three core decisions: gear family (helical, bevel-helical, planetary), torque class (up to 2,495,900 lb-in for top-end industrial units), and duty-cycle rating (service factor 1.5–2.5 for cutter heads). Match the reducer to motor speed, shock load, and thermal limi

Worm gear reducers fit textile mills as a cost-effective right-angle option for low-duty auxiliary drives, but efficiency below 70% and 10,000-50,000 hr life require pairing them with helical sets on main lines. Selection centers on ratio range, duty cycle, ambient lint, and thermal envelope.

For automotive production lines, worm gear reducers fit conveyor, indexing, and low-speed robotic axes where right-angle layout, self-locking hold, and ratios of 20:1 to 60:1 matter more than peak efficiency. Select by torque, ratio, mounting, sealing, and continuous-duty thermal class; expect 30% t

Worm gear reducers in pulp and paper plants are specified for self-locking, high single-stage ratios (commonly 60:1 and above), and right-angle mounting on auxiliary duties such as edge-trim nozzle adjustment, refiner drives, pulper drives, and dryer section positioning. Select a worm unit only when

Worm gear reducers remain the default spec for most agricultural-machinery drives: compact right-angle layout, ratios from 5:1 to 3000:1, self-locking, and 50-80% efficiency. Selection must lock working load, torque, mounting space, and duty before choosing NMRV, WP, or helical-worm (S-series) housi

For marine deck machinery, right-angle worm gear reducers are commonly specified for windlasses and capstans, delivering single-stage ratios from 5:1 to 60:1 at 52-93% efficiency; choose sealed cast iron housings, bronze worm wheels, and verified self-locking for chain-handling safety.

Worm gear reducers for wind power are limited to yaw, pitch, and auxiliary drive duties where self-locking, right-angle output, and single-stage ratios of 10:1-60:1 matter more than efficiency (40-85%). Main rotor drivetrains in 2026 use planetary or helical gearboxes at 94-98% efficiency instead.

Worm gear reducers dominate material handling because single-stage ratios of 5:1 to 100:1 fit most conveyor, hoist, and turntable loads. Self-locking behavior emerges above ~60:1, but efficiency drops from 85–90% at 5:1 to 35–52% at 80:1, so thermal rating drives the final pick.

Worm gear reducers are the go-to right-angle drive for packaging lines, with typical ratios of 5:1 to 80:1, output torque from 8 Nm to 250 Nm, and input power 0.09-1.5 kW for sub-1.5 kW labelling and cartoning duty. Sizing starts from running torque times a 1.25-2.5 service factor, then de-rates abo

Worm gear reducers fit food processing when compact right-angle drives, 10:1 to 60:1 ratios, and self-locking hold are required, but their 40 to 85 percent efficiency and heat output rule them out for high-torque conveyor lines. Choose aluminum-housed units for washdown zones under 7.5 kW; switch to

Worm gear reducers deliver single-stage ratios from 5:1 to 100:1 in compact right-angle housings with 40–90% efficiency, making them the practical pick for mining hoists and conveyors where self-locking, shock load tolerance, and footprint matter more than continuous-duty efficiency.

Planetary reducer selection for automotive production lines centers on four spec gates: peak vs continuous torque, backlash class, IP rating, and ratio architecture. Frame sizes 60-180 mm cover 200 W to 11 kW servo motors, and a 1.2-2x service factor on rated output torque is the minimum engineering

For pulp and paper mill drives, planetary reducers with helical gearing, ≥95% mechanical efficiency, IP55 sealing, and torque ratings of 57–6,700 kNm cover the bulk of refiner, calender, and reel drum applications. Specify sealed oil-lubricated housings with stainless output hardware and verify AGMA

Agricultural machinery typically pairs planetary reducers with diesel engines in the 1.5-15 kW range at ratios of 10:1 to 40:1 for PTO, wheel-drive, and feeder-roller duty, while worm reducers fit only low-duty, intermittent conveyor or mixer loads where self-locking and cost matter more than effici

Planetary reducers dominate wind turbine drivetrains because they deliver the highest torque density per kilogram in a coaxial envelope, making them the default for main rotor, yaw, and pitch stages. Selection hinges on reduction ratio, torque rating, backlash class, bearing support, and gearbox con

For material handling, planetary reducers in the 3:1 to 1000:1 ratio range and 94-98% efficiency class are the strong default when a coaxial layout, high torque density and low backlash are required; helical-bevel or hypoid units win only when shaft geometry, ratio window, or cost rules out a planet

Planetary reducers are the default pick for steel mill drives because they pack 94-98% efficiency, coaxial input/output, and 3:1 to 1000:1 ratios into a compact housing that survives rolling-mill shock loads. Selection hinges on torque density, ambient heat near furnaces, and matched duty cycle, not

Helical-bevel, parallel-shaft, worm and planetary gearboxes from 0.12 kW to 200 kW are the four families specified for spinning, weaving, carding and finishing lines; selection hinges on torque density, lint-tolerant sealing (IP54 to IP65), noise ceiling (60 to 78 dB at 1 m), and ISO 6 gear-grinding

For automotive production gearboxes, start from a written duty profile (continuous and peak N·m, rpm, duty %, temperature, envelope, fluid compatibility) before matching topology: helical for manual/DCT at M1.75–M3.5 and AGMA 11–12 quality, planetary for shift actuators and EV reduction, hypoid for

Marine gearbox selection turns on three numbers: engine kW, target propeller RPM, and required reduction ratio. Reverse-only units suit 1:1 small craft; reduction gearboxes step main-engine speed from 1,500-2,000 RPM down to 100-300 RPM at the propeller, with double-helical units rated to 50,000 kW

Wind turbine gearbox selection hinges on matching torque, ratio, and topology to site conditions: planetary stages absorb 5–20 RPM rotor input at 4:1–6:1, multi-stage drivetrains dominate utility-scale fleets, and replacement demand is set to outpace new-build demand in late-decade projections (USD

Conveyor and feeder gearbox selection in 2026 hinges on four inputs: motor RPM, output RPM at the head pulley, conveyor archetype with daily duty hours, and shock-load character. Specifying to AGMA 6034 service factor (1.4-2.0), ratio brackets per ISO 6336 stage count, and verified thermal-plus-over

Selecting a gearbox for a packaging line means matching torque, backlash, speed ratio, and washdown rating to each station rather than buying one unit for the whole line. Worm units fit low-duty conveyors, helical-bevel and planetary units cover most mid-range indexing, and harmonic or low-backlash

Helical, bevel-helical, worm and stainless-steel washdown gearboxes are the four mainstream choices for food-processing lines in 2026, selected around output speed, torque, cleaning environment and maintenance access rather than motor power alone. For mixers, conveyors and packaging cells,

Steel mill gearboxes need service class III (AGMA 2.0+), IP65/66 sealing, and housings rated above 60-80C ambient, with helical or planetary units most common across rolling, cooling-bed, and conveyor duty.

Cement-plant gearbox selection hinges on duty cycle and service environment: DBY/DCY bevel-helical units per JB/T 9002-1999 cover belt conveyors, while kiln drives need IE5 motors and 3-month oil analysis under heavy load.

Helical, bevel-helical, and planetary gearboxes dominate mining duty, with selection driven by shock load, service factor, and ambient dust. Planetary units now reach 1,500 kW ball-mill class with multi-megawatt conveyor drives expanding on the same platforms.

Textile mills need slewing bearings sized for slow indexing rather than continuous high speed: pick a 4-point contact or crossed-roller slewing ring with sealed raceways, verify axial and radial load ratings against the heaviest fabric roll, and confirm corrosion protection for humid, lint-laden pla

Automotive production lines specify slewing bearings by four-point contact, cross-roller, three-row roller, or double-row ball type, selected on static load capacity, combined axial-radial-moment load envelope, and mounting rigidity rather than fatigue life alone.

Slewing bearing selection for pulp and paper hinges on four-axis load, sealing against fiber/liquids, corrosion-resistant materials, and verified 4-point contact or crossed-roller geometry from established OEM lines like Schaeffler XU series, sized against application-specific dynamic/static ratings

Agricultural slewing bearings are large-diameter raceway assemblies (typically 200–6,000 mm bore) selected on static load, moment capacity, seal grade and gear option, with 42CrMo4 raceways hardened to HRC 55–62 and IP65/67 sealing preferred for dust, slurry and field-spray exposure.

Marine slewing bearings are typically specified as 011/012 external-gear or 013/014 internal-gear four-point contact ball units for knuckle-boom and deck cranes, with double-row ball or three-row roller structures selected for hose-handling and offshore heavy-lift duties, and all rings require docum

Material-handling slewing bearings are typically specified in the 200-6,000 mm diameter range, with four structural families (single-row four-point contact ball, crossed roller, double-row ball, three-row roller) covering light-duty manipulators through 6 m port-crane rings. Selection must balance a

For packaging-line slewing bearing selection, specify a four-point contact ball or crossed-roller unit in the 200–600 mm bore range with 42CrMo4 or 50Mn rings, raceways induction-hardened to 55–62 HRC, and IP65 sealing. Match type to load profile: balls for combined axial/radial/moment, rollers for

Steel-mill slewing bearings are heavy-duty three-row roller or crossed roller units, typically 1,500–4,500 mm in diameter, built from 42CrMo or 50Mn rings hardened to HRC 55–62 for ladle turrets, continuous casters, and rolling-mill tables.

Slewing bearings in cement plants are typically selected as four-point contact ball or crossed roller units sized for combined axial, radial, and tilting-moment loads on kilns, preheaters, and stacker-reclaimers. Selection is driven by load case, raceway hardness, sealing against cement dust, and ge

Mining-duty slewing bearings are large-diameter rolling-element rings, 200 mm to 6,000+ mm bore, that carry axial, radial, and overturning-moment loads simultaneously. For excavators, stacker-reclaimers, and rotary dump trucks, selection hinges on static load capacity, structural rigidity, raceway h

Slewing ring bearings for textile mills must carry combined axial-radial loads at slow to moderate rotational speeds, while resisting lint ingress, humidity, and 24/7 duty cycles. Crossed-roller and double-row angular-contact designs in the 400-500mm diameter range are the common selection, sized vi

Slewing ring bearings for pulp and paper must combine corrosion-resistant sealing, moment load capacity, and 1–3° self-alignment to survive humidity, chemical exposure, and continuous dryer-section heat up to 80°C. Match crossed-roller, ball, and triple-row types to specific machine sections for rel

Marine slewing ring bearings must combine 42CrMo4 or 50Mn induction-hardened rings, 55-62 HRC raceways, and IP66+ sealing to survive saltwater, while four-point ball, crossed roller, or three-row roller designs cover the 200-6000 mm diameter range and the under-50 RPM operating envelope of offshore

Slewing ring bearings for material handling span 200–6,000 mm diameters and four structural types: four-point contact ball, crossed roller, three-row roller, and double-row ball. Selection hinges on simultaneous axial, radial, and tilting-moment loads, with downtime costs of $50,000–$200,000 per cra

Slewing ring bearings on packaging lines are typically selected in the 200–600 mm diameter band as four-point contact ball or crossed-roller units, with 50Mn or 42CrMo forged rings, HRC 55–62 raceways, and integral gear teeth driven by a worm or servo.

Food-grade slewing ring bearings for processing lines need stainless or coated rings, food-grade H1 grease, IP66+ sealing, and 200-5000mm diameter sizing. A four-point contact ball or crossed-roller design is the common spec for washdown-rated rotary tables and fillers.
Conveyor chain pricing in 2026 is driven by pitch, attachment K1/K2 spec, material grade and lot size; verified manufacturer pages show active quoting at FB Chain, Shinelink, Dongchuan and ESBEE on 2026-06-28.
Harmonic drive (strain wave gear) reducers are zero-backlash, single-stage units with ratios of 30–160, used on robot axes and precision servo systems. Installation hinges on correct flexspline orientation, lubrication schedule, and torque-anchor preload per OEM data sheet.

Steel-mill slewing ring bearings are typically specified in the 1,500–4,500 mm diameter band, with three-row roller designs preferred for ladle turrets and continuous-caster turntables that carry combined axial loads above 2,000 kN and continuous tilting moments. Material is almost always 42CrMo4 (o

Slewing ring bearings for cement plants must combine high overturning-moment capacity (often above 50,000 kN·m at large diameters), sealed raceways against cement dust, and integrated gearing sized to kiln/preheater duty cycles.

Hybrid ceramic bearings (steel races with silicon nitride or alumina balls) suit high-speed textile spindles and dyeing equipment, while full ceramic bearings target chemical-laden wash zones. Selection hinges on speed, load, temperature, and lint/moisture exposure.
For automotive production lines, specify silicon nitride (Si₃N₄) hybrid ceramic ball bearings for EV traction motors, turbochargers, and wheel hubs; reserve full ceramic (ZrO₂ or Al₂O₃) only for chemically aggressive or electrically isolated subassemblies where shock loads stay low.
Ceramic hybrid bearings with silicon nitride rolling elements and 440C stainless steel rings are now the mainstream specification for pulp-and-paper wet-end and dryer sections, cutting lubrication-related failures by 4x versus standard all-steel deep-groove designs. Selection on paper machines is di
Ceramic hybrid bearings suit combine harvester engines and high-heat tractor zones; full Si3N4 or ZrO2 units fit corrosive paddy and fertilizer zones. Pick ceramic hybrid for the high-temp load, not as a universal upgrade over chrome steel.
For wind power, hybrid silicon nitride (Si₃N₄) ceramic-rolling-element bearings are the credible choice when main-shaft, gearbox and generator nodes need 20+ year maintenance-free life; full-ceramic rings remain niche due to brittleness under pitch impact loads.
Ceramic bearings split into full ceramic (ZrO2, Si3N4, Al2O3) and hybrid (ceramic balls + steel rings), with full ceramic rated up to 1600°C and zirconia covering pH 1–14. For material handling, hybrid Si3N4/GCr15 typically wins on toughness and DN value; full ceramic is reserved for corrosive, non-

Silicon nitride hybrid ceramic bearings (steel rings + Si₃N₄ balls) are the practical default for high-speed packaging-line spindles, conveyors, and filling-machine agitators, where 400,000 rpm-class speeds, washdown exposure, or inverter-driven stray currents would shorten steel-bearing life. Full-

Full ceramic (Si3N4 or Al2O3) bearings are the preferred fit for food-processing washdown zones, where their chemical inertness and dry-running capability outperform 440C stainless and hybrid designs that still expose steel raceways to cleaning agents.
Marine linear actuator selection hinges on IP66/IP67 sealing, a 20-30% force safety margin, and 316 stainless hardware, with electric units preferred for hatches and hydraulics for high-load subsea valves.
Steel-mill work rolls, continuous-caster segments, and hot-strip coilers run at 200–600°C with water and scale contamination, where hybrid silicon nitride (Si₃N₄) ceramic bearings on 52100 or M50 steel raceways are the dominant 2026 upgrade. Full Si₃N₄ or zirconia sets are reserved for acid/corrosiv

Hybrid ceramic bearings are specified for cement plant motors and ID fans where electrical erosion is a known risk, with silicon nitride rolling elements paired with steel rings for VFD-driven equipment. Spherical roller bearings remain the default for kiln support rollers, mill trunnions, and crush

Silicon nitride and zirconia hybrid bearings cut rotating mass, resist corrosion, and survive dry/wet contamination better than 52100 chrome steel in mining service. Spec for 250°C+ zones, abrasive slurry, and electrical-isolation duty with hybrid Si3N4 balls plus PTFE or graphite cages.

Spherical roller and spherical plain bearings dominate pulp and paper applications from pulper rotors to dryer cylinders, with TL-series case-hardened SRBs rated to 200°C and self-aligning SRBs tolerating 0.5°-1.5° shaft deflection per current OEM guidance.

Spherical plain bearings in agricultural machinery must be selected for oscillation, shock load, and contamination, not for high speed. Steel/steel radial types with seals suit tillage and implement lift points; PTFE-lined maintenance-free types suit pivot pins inaccessible to grease. Selection hing

Spherical plain bearings for wind turbines are specified for pitch and yaw oscillating joints, blade pitch hinges, and yaw drives, where misalignment tolerance and slow oscillation dominate. Selection hinges on load rating, sliding contact type, lubrication regime, and corrosion resistance.

Spherical plain bearings are the right fit for packaging-line pivots, swing arms, and indexing cams where misalignment up to about 2 degrees and oscillating motion dominate. Match on load direction, oscillation angle, and lubricant compatibility, not just bore size, to avoid premature wear.

For food processing, select radial spherical plain bearings in 304 or 316 stainless with food-grade H1 grease, PTFE-lined maintenance-free sliding layer, or solid-lubricant composite when relubrication is impractical. Match the model code to load direction, sliding surface, seals, and NSF/ISO 21469

Spherical plain bearings are the spec-first choice for cement plant trunnions, kiln supports and crusher shafts: misalignments up to 1-3°, dust-laden ambient to 220°C, and combined radial/axial loads define the 2026 selection rules.

Spherical plain bearings for mining operations should be selected by load direction (radial, angular contact, thrust), sliding-surface family (steel/steel vs PTFE composite), and bore size from 20 mm up to 1,400 mm; misalignment tolerance typically reaches 1.0 to 2.5 degrees, and mining duty cycles
UCP-series cast-iron pillow block bearings with UC insert ball bearings are the default pick for textile-mill shaft supports; stainless or thermoplastic housings are specified only where washdown, lint-laden humidity, or chemical exposure justify the premium.
Automotive production lines typically specify 2-bolt UCP200/UCP300 insert-bearing pillow blocks in cast iron or pressed steel, with shaft diameters 12-75 mm, dynamic load ratings 9.88-47.5 kN, and self-alignment of ±2° to ±5°. Selection pivots on six engineering variables: shaft fit, load type, envi
Pillow block bearing selection for pulp and paper hinges on matching insert type, seal design, and housing material to the section of the machine, with spherical roller pillow blocks dominating dryer, calender, and press rolls. NSK's TL-Series steel, rated for 200°C dimensional stability, and Timken
Pillow block bearing selection for agriculture machinery centres on cast-iron or pressed-steel housings (UCP/UELP series) with UC insert ball bearings and triple-lip seals, matched to shaft bores of 20-50 mm and loads commonly seen on conveyors, augers, and PTO drivelines.

For marine duty in 2026, specify 316 stainless or thermoplastic pillow block bearings with IP66 seals and H1 grease; avoid HT150 cast iron housings and standard nitrile seals on deck equipment. Match housing grade, insert type, and sealing to salt-spray exposure, not catalog price.

Wind turbine pillow block bearing selection in 2026 centres on heavy-duty plummer blocks with spheroidal graphite iron housings, split-tapered roller inserts, and relubrication-friendly seals rated for nacelle thermal swings from -20°C to +60°C. Source confirms split pillow block housings paire

Pillow block bearing selection for material handling hinges on matching bore, housing style, insert series, and seal class to load and contamination. UCP/UCF/UCFL/UCFC housings cover most conveyor and roller needs.

Pillow block bearing selection for packaging lines hinges on shaft size, load rating, seal type, and material, with UCP, UCF, and UCFL series covering most conveyor and filler shaft applications from 12 mm to 90 mm.

For food processing lines, specify stainless steel (304/316) or thermoplastic/PBT pillow block bearings with H1 food-grade grease, IP66+ sealed inserts, and UCP/UELP series bores from 20 mm to 40 mm; avoid painted cast iron in washdown zones.
Steel mill pillow block bearing selection hinges on three concentric steel-mill load cases: continuous caster segment rollers (heavy shock, scale, 150-200°C), runout table and hot strip mill rolls (water/scale, 200-350°C peaks), and conveyor/auxiliary shafts (dust, ambient, light shock). Use cast-st
Tapered roller bearings for pulp and paper machines must combine heavy radial load capacity, shock tolerance, and corrosion-resistant sealing to survive wet, contaminant-laden environments. Selection hinges on four criteria: dynamic load rating, limiting speed, seal design, and lubrication regime ma

Tapered roller bearings, governed by ANSI/ABMA 19.2:2013 for inch series, are the workhorse radial+axial load carriers on tractors, combines, and tillage gear. Spec the right cone/cup pair, sealing class, and fitting practice first; dynamic load rating and contamination control decide service life i

Wind turbine main shafts and gearboxes target a 175,000-hour bearing life (20 years), forcing tapered roller bearing selection beyond catalog methods. Load-zone slicing, ISO 281 modified reference life, and corrosion-resistant sealing are the non-negotiable spec criteria for both onshore and offshor

Tapered roller bearings for material handling are typically single-row, inch-taper chrome-steel units in P0/P6/P5 precision, sized from 70 mm bore (33114) to 85 mm bore (32217), selected on radial+axial load, CEMA idler class, sealing, and contamination exposure.

Tapered roller bearings in packaging lines are most often single-row metric series (30200, 30300, 32000, 32200, 32300) sized by combined radial+axial load, 1.5-3.0 kW drive class, and 10-30 r/min roller-shaft speeds; correct selection matches cup/cone part numbers to ISO 15:2017 and avoids mis-apply

Tapered roller bearings are not a default fit for food processing lines: stainless or polymer-caged variants with H1 food-grade grease and IP66+ sealed housings are required where washdown, caustic cleaners, or low pH product contact occur. Spec the bearing to the shaft, the seal to the washdown che

Steel-mill tapered roller bearing selection is governed by row count, bore range, and lubrication path. For 2026 sourcing, four-row SRNB covers 195.0–710.55 mm bores, while TQOW spans 50.8–1499.87 mm bores. NSK Molded-Oil variants suit corrosive mill zones with maintenance-free operation.

Self-aligning ball and spherical roller bearings are the two structural choices for textile-mill shafts running at 0.5°–2° misalignment, with seal material, lubrication interval, and lubricant-grade limits set by ISO 15:2017 and plant fibre/fly load. Pick sealed 2RS variants for ring-spinning and hu

For marine propulsion and deck machinery, double-row self-aligning ball bearings (1200/1300/2200/2300 series) are the default pick when shaft deflection and hull-flex misalignment exceed roughly 1.5 to 2.5 degrees; spherical roller variants handle heavier radial and shock loads above 100 kN.

Self-aligning bearings for wind turbine main shafts, gearboxes, and pitch/yaw drives are selected from spherical roller (high radial load, misalignment up to 1.5–2.5°) or self-aligning ball (lighter, misalignment up to 2.5–3°) types, with sealing, grease, and clearance matched to ISO 492 and IEC 614

For material-handling conveyors and feeders, self-aligning ball bearings (1200/1300/2200/2300 series) suit light shafts, while spherical roller bearings such as 22220CA-22226CA carry higher radial loads on heavy conveyors. Selection should be based on misalignment tolerance, load, speed, and sealing

Self-aligning ball bearings with 25-62 mm bores, polyamide cages, and C3 clearance are the standard fit for packaging-line conveyor and filler shafts, with 14000 rpm limits on 25 mm bore units. Selection hinges on misalignment tolerance, cage material, IP sealing, and food-grade lubricant compatibil

Self-aligning bearings for food processing must pair stainless 304/316 rings with H1 food-grade grease and solid cage materials; misalignment tolerance of 1.5–3° is the decisive spec for washdown conveyor and mixer shafts. Validate against NSF/ANSI 169, FDA 21 CFR 178.3570, and ISO 22000 food-safety

Self-aligning bearings in steel mills use spherical outer-race geometry to absorb shaft deflection and misalignment of 1.5 to 3 degrees, with spherical roller types preferred for roll-neck and continuous-caster applications. Selection hinges on load rating, contamination sealing, and lubrication reg

Self-aligning ball and spherical roller bearings with ±2.5°–5° misalignment tolerance and 22200/22300 series designations are the default spec for cement-plant conveyors, kilns, and grinding mills, per OEM catalogues and Springer Tribology Encyclopedia.

Self-aligning bearings, in ball and spherical-roller variants, compensate 1.5° to 3° of static misalignment typical in mining conveyors, crushers, and vibrating screens. Selection hinges on load type, contamination sealing, and clearance class rather than bore size alone.

Angular contact bearings for textile mills must combine high radial and axial load capacity with contamination-resistant sealing and 15° to 40° contact angles to handle high-speed spindles, draft rollers, and loom sundry parts.

Angular contact bearings for automotive production are selected by matching contact angle (15°/25°/40°), cage material, and bore series to load and RPM; 7000/7200/7300 series dominate hub and transmission duty, with 40BD219 air-con units and 7202 automotive grades widely quoted in 2026 sourcing data

Single-row angular contact ball bearings, typically arranged in DB or DF matched pairs, dominate combine and tractor gearbox applications, with agriculture-grade units from CYSD and similar mills rated 100,000 pieces/month capacity and US$1-20 FOB price points.

Angular contact bearings for marine duty must combine matched-pair mounting, contact angle of 25-40 degrees, and marine-grade corrosion protection; double-row or four-point types handle bidirectional thrust in propeller shafts.

Angular contact bearings for wind turbine main shafts and gearboxes are typically specified in matched sets with 30° to 40° contact angles, commonly in 7200B/7300B or matched 7000C/7200C series per JTEKT Koyo catalog data. Selection revolves around combined radial-plus-axial load capacity, grea

Angular contact bearings for material handling must combine duplex back-to-back arrangements, contact angles of 25 to 40 degrees, and ISO 15 or ABEC-5 minimum tolerance, with grease life matched to 20,000 hour L10 targets. NTN's 7314BDB duplex series exemplifies this configuration for conveyor and h

Angular contact bearings for packaging lines should be selected by contact angle, paired mounting arrangement, and lubrication protocol rather than by bore size alone. The 30/40° contact angle split and DB/DF/DT pairing rule govern axial load capacity and packaging-line spindle stiffness, and 7000/7

Angular contact bearings for food processing must combine stainless or ceramic materials, food-grade lubrication, and sealed contact-angle geometry rated for combined radial-axial loads. Selection gates for 2026 prioritize IP69K washdown sealing, FDA-compliant lubricants, and 440C/ceramic hybrid con

Angular contact bearings for steel mill work rolls and backup rolls must be specified by contact angle (15/25/40 deg), paired mounting arrangement (DB/DF/DT), and P4-P2 precision class. Verified supply range on 2026-08-11: 20mm bore super-precision ABEC-7 units at US$21-99 retail, mid-series 7020-72

Angular contact bearings for cement plants must be selected by contact angle (15/25/40 deg), cage material, sealing, and precision class, with paired mounting typical for high-radial kiln and mill loads. Matched 7000C/AC series pairs with brass or PEEK cages dominate raw-mill and crusher duty at ope

Angular contact bearings for mining duties must be specified in matched sets with 30°–40° contact angles, ABEC-3 or tighter tolerances, and sealed or shielded units to survive dust, vibration, and shock loads common to crushers, conveyors, and dump trucks.

Textile-mill linear bearing selection hinges on matching the LM bushing or slide rail to lint exposure, wash-down chemistry, and high-cycle reciprocating loads. Round-rail plain bushings fit low-speed frames; sealed ball-bearing pillow blocks handle loom reeds up to 5,000 lbf dynamic.

Linear bearings for automotive production lines fall into three families: polymer plain bushings, round-rail ball bushings, and profile-rail (square) recirculating units. Round-rail ball bearings handle dynamic loads up to 5,000 lbf at diameters 0.25–4 in; plain polymer bushings cover lighter duty a

Pulp and paper mills specify linear bearings against four hard gates: 440C/52100 bearing steel, IP65 or higher sealing, 80-200°C continuous rating, and 17-25 kN dynamic load per 25 mm shaft. Cross-roller and stainless variants win on corrosion, polymer-lined bushings win on chemical washdown, recirc

Linear bearings for marine duty must pair stainless or polymer-caged bushings with 440C/316 shafts, IP65+ housings, and grease rated for salt fog. Common failures come from washout and crevise corrosion, not from base load rating.

Linear bearing selection for material handling hinges on matching bushing type, load rating, shaft hardness, and sealing to the duty cycle, with recirculating ball and plain-bearing families dominating conveyor, lift, and AGV/AMR spec sheets in 2026.

Linear bearings on packaging lines fail most often from contamination, washdown chemistry, and stroke-speed mismatch, not from basic load rating. Select by closed-versus-open architecture, cage or non-cage design, lubrication class, and IP sealing before any dynamic load number. Match the bearing fa

For food processing lines, linear bearing selection hinges on three gates: lubrication strategy, corrosion resistance, and cleanability. Polymer sliding guides and stainless recirculating ball bearings now dominate wet and washdown zones, with food-grade polymer liners eliminating grease contaminati

Linear bearing selection for steel mills is dominated by four-row profile roller guides, crossed-roller slides, and sealed ball bushings, rated for ambient temperatures from 80°C to 200°C with IP54–IP67 sealing and grease intervals of 3,000 to 6,000 hours. Spec gates center on dynamic load rating, l

Cement plants expose linear bearings to abrasive dust, 150°C+ ambient zones, vibration and water splash, so the workable envelope sits inside plain polymer bushings on unhardened shaft, sealed profile-rail blocks with EP2 grease, or polymer-glide rail with stainless shaft. RoundRail polymer bushings

Mining-duty linear bearings are typically round-rail ball bushings or polymer plain bushings on induction-hardened 52100 or case-hardened shafting, selected first on load case (kN) and dust/water ingress, then on speed and stroke. For shovels, dump trucks, and underground drills, sealed caged-ball s
Thrust bearings in textile mills take axial loads from ring frames, printing calenders, and stenter chains, with selection driven by load, speed, lubrication, and lint contamination rather than catalogue price. A 2026 field spec map aligns bearing type, sealing, and lubrication choice with the dust

Thrust bearing selection for automotive production lines centres on four decision gates: load type (axial vs combined), speed class, lubricant regime, and housing fit. Chinese tier-2/3 plants (BYD, Man Wah, Elec-Tech) source thrust ball and needle roller units from GCr15 chrome-steel suppliers such
Thrust bearing selection for tractors, planters, and combine harvesters hinges on matching ball vs roller vs spherical thrust types to axial load, dust ingress, and ISO 9001 supplier discipline, with Chinese OEM catalogues now offering agriculture-rated lines side-by-side with general industrial sto

Marine propulsion thrust bearings fall into two main duty classes: white-metal tilting-pad for high-load, high-speed shaftlines, and permanent-magnetic or rolling-element variants for special cases. Selection gates in 2026 are load capacity, lubrication architecture, and class-society materials comp

Wind turbine main-shaft thrust bearings for 3-6 MW units are dominated by rolling-element spherical roller and tapered roller types, sized from 1.0 m to 1.5 m bore, with L10 life targets of 130,000-175,000 hours. Tilting-pad hydrodynamic bearings remain the heavy-load alternative above 5 MW at slow
Thrust bearing selection for material handling pivots on axial load, shaft speed, alignment tolerance, and contamination exposure. Match bearing type to application: ball thrust for light high-speed, cylindrical roller thrust for heavy combined loads, spherical roller thrust for misalignment up to 1

Thrust bearing selection for packaging lines hinges on four spec gates: axial load class, rotational speed, lubrication regime, and wash-down rating, with YRT-style combined axial/radial units dominating indexing tables and SKF/NSK/Schaeffler-class cylindrical or angular-contact designs serving conv
Thrust bearings for food processing must combine sanitary stainless construction (typically 304/316), food-grade H1 or NSF H1 registered grease, IP65+ sealing, and ability to handle washdown chemicals like sodium hypochlorite and hot CIP fluids up to 90 degrees Celsius, while supporting the high axi

Cement plants need heavy-duty thrust bearings for kilns, mills, and crushers; selection hinges on axial load capacity, contamination sealing, and lubrication type, with tilting-pad and roller designs dominating the 2026 spec map.

Mining-duty thrust bearings are typically specified as either tilting-pad hydrodynamic units or rolling-element types, with selection driven by axial load, RPM, alignment tolerance, and lubrication availability at the mill or shovel site.

Textile-mill roller bearing selection runs on four criteria: shaft speed, radial load, contamination exposure, and misalignment tolerance. Spherical, tapered, and cylindrical types each cover a defined duty band; GCR15 chrome steel remains the baseline material, with seals and lubrication deciding r

Roller bearing selection for automotive production hinges on matching bearing type to load case: deep-groove ball for wheel-hub duty, tapered roller for transmission, cylindrical for high-RPM spindles. Tolerance class P5-P6 and ISO9000/ISO14000-certified supply are the current 2026 minimum gates.
Roller bearing selection in pulp and paper mills maps to four machine families: press rolls, dryer sections, calender stacks, and corrugating/winder drums. Match bearing type to load vector, speed, wash-down exposure, and ISO 15 L10 life, then choose seal and lubrication to the section.
Agricultural-machinery roller bearing selection in 2026 hinges on three gates: sealed-unit contamination rating, dynamic load rating per ISO 15, and conformity to IATF 16949 for OEM drivetrains. Sealed disc-harrow, tillage, and baler bearings dominate the segment, with tracked ag-vehicles driving de

Marine roller bearing selection is driven by saltwater corrosion, sustained radial+thrust loads, and class-society approval: spherical roller and cylindrical roller bearings dominate marine gearboxes, rudders, and propeller shafts, with 42CrMo rings, nitrile or PTFE seals, and DNV/ABS/LR certificati

Wind turbine main-shaft and gearbox bearings are selected by rotor load, L10 life target, and lubricant regime, with spherical roller bearings dominant for rotor and main shaft and tapered roller bearings dominant for planetary gear stages. Specifiers verify ISO 76/281 ratings, ISO 4406 oil cleanlin

Roller bearing selection for material handling hinges on matching load type, RPM, contamination exposure, and mounting style to one of four families: deep-groove ball, cylindrical, spherical, and tapered. Bulk wholesale tapered units are listed from US$9-10 per set on Made-in-China with 800,000-set

For packaging-line roller bearing selection in 2026, match bearing type to the line station: deep-groove ball bearings for general conveyor idlers, cylindrical roller bearings (NU/NJ/NUP series) for high-radial-load nip and forming rolls, and tapered roller bearings for combined radial+axial film, c
Steel-mill roller bearing selection in 2026 hinges on four-row cylindrical, sealed spherical roller, and CARB toroidal designs rated for 200-350°C work-roll and continuous-caster service. Match type to station, then verify clearance class, lubrication regime, and mounting clearance against ISO 15:20

Cement plants push roller bearings through extreme contamination, heat, and impact loads, so selection hinges on four bearing types: spherical, cylindrical, tapered, and needle roller. Use spherical for kiln and crusher misaligned shafts, cylindrical and tapered for high-radial mill gearboxes, needl
Spherical roller bearings and tapered roller bearings dominate mining duty-cycles from 2026, paired with crossed-roller units in mill gearboxes; selection hinges on dynamic load rating, contamination sealing, and profile modification, with 90° roller crossover delivering combined axial-radial-moment

Textile mill spindles, drafting rollers and looms run hot, dusty and humid, so 6200/6300-series sealed deep-groove ball bearings with ZZ or 2RS closures dominate the spec. For high-speed ring spinning above 18,000 rpm, ABEC-5 hybrid ceramic or high-temperature grease options extend relube intervals

Pulp and paper mills specify ball bearings on four hard gates: corrosion resistance to acidic/alkaline stock and chlorides, 150-180°C dryer-section thermal headroom, water/steam washdown sealing to IP65-IP69K, and AFSMA-mount series fit (6200/6300 for fans, 22200 for presses). Sealed 2RS or 2Z chrom
Sealed deep-groove and insert ball bearings in the UC200/UCP200 series dominate agriculture-machinery selection, with US$0.50–10/piece FOB pricing across 60+ Chinese factories as of 2026-08-09, subject to dust, moisture, and shock loads that demand robust contact seals and grease retention.

Marine ball bearing selection centres on corrosion-resistant materials (stainless 440C/316, ceramic Si3N4), C3/C4 internal clearance, 2RS or 2RZ sealed contacts, and class I/II ABS or DNV-GL approval for hull, deck machinery, and propulsion auxiliary service.

Wind turbine main-shaft and gearbox bearing selection hinges on four-point contact and slewing ball bearing variants with 1.5-3.5 m diameters, 100Cr6 chrome steel balls, and rated lives above 175,000 hours under variable axial-radial load.

Ball bearing selection for material handling hinges on matching bearing type, seal class, and material to load, speed, contamination, and washdown duty. Spec deep groove chrome steel for general conveyor rollers, switch to stainless or hybrid ceramic where corrosion, chemicals, or temperature rule o

Ball bearing selection for packaging lines is driven by four spec gates: shaft speed class, lubricant/food-grade compliance, seal type, and cage material. Match bearing series to duty cycle, not catalogue price, on conveyors, fillers, and labellers.

Steel mill bearing selection pivots on four load/heat thresholds: pick deep-groove ball bearings up to 6200-series for roll-table idlers, sealed ceramic-hybrid units above 200 °C, and roller types once radial loads exceed 50 kN. Match clearance to shaft fit, not catalog defaults.

Cement-plant ball-bearing selection is dominated by spherical roller and sealed deep-groove types in 222xx/223xx series, with operating temperatures typically 150-200°C at kiln and preheater fans.

Selecting ball bearings for mining requires matching sealing class, lubrication, and material to dust, shock, and contamination. Deep groove, spherical roller, and sealed variants serve different load and misalignment duties on-site.
Shaft couplings connect a driving shaft to a driven shaft, transmitting torque while absorbing parallel, angular, and axial misalignment. Selection pivots on torque, speed, misalignment budget, damping, and environment, with rigid, flexible, and torsionally-soft elastomeric types each matched to spe

Wire rope slings are the dominant high-tonnage rigging option in steel mills, ports, and offshore platforms, with seven standard configurations covering 0.5-1,500 tonne working loads. Selection is governed by sling geometry, end-fitting type, and the ASME B30.9 duty cycle of the lift, not by the rop

Industrial spring sourcing in August 2026 splits into three regional clusters: China (Songjiang/Shanghai, Langfang/Hebei, Zhongshan/Guangdong) leading on custom wire forming and SUS304 tension springs from US$0.01-0.99/piece, India (Rajkot, Ahmedabad, Mumbai) dominating heavy-duty compression, disc,
Bucket elevators move flowable bulk material vertically, with three main types: centrifugal discharge, continuous, and positive discharge, each covering a defined particle-size and capacity band. Selection hinges on material density, lump size, abrasiveness, lift height (up to 200 m on belt units),

Pneumatic conveyors move dry bulk through sealed pipelines using air or inert gas, while chain conveyors pull solid unit loads or pallets along a rigid track. Pneumatic systems fit dusty, explosive-risk, or multi-direction vertical plants; chain conveyors win on heavy payload, lower air cost, and me

China-based pneumatic conveyor suppliers dominate the global Sourcing map, with 2,000-plus verified manufacturers on made-in-china.com and pneumatic conveying systems on offer from dedicated plants in Vadodara, Zhangjiagang, and Zhengzhou at FOB price points from US$15 per piece to US$10,000 per set
Screw conveyors and conveyor chain systems move bulk solids through fundamentally different mechanisms, so the choice between them is set by material abrasiveness, incline angle, temperature, and whether the line needs sealed or sanitary operation. Screw conveyors win on sealed, short-distance horiz
Chain conveyor and conveyor chain are not interchangeable terms: one is a bulk-material handling machine (AUMUND type PKF/TKF, closed-trough, up to 3.5 bar shock-pressure rated), the other is a transmission component (DIN/ANSI/GB/T standard sizes 08B-16B, US$1.5-2/meter FOB) that drives conveyors, p

Chain conveyors split into five operating families: double-strand, center, vertical, plate, and tubular drag, each matched to load, geometry, and hygiene. Selection hinges on conveyed material, route geometry, sanitation class, and abrasive wear, not on a single tonnage figure.
Roller conveyors suit flat-bottomed unit loads at 5-60 m/min on gravity or powered lines, while conveyor chains carry heavy, hot, or oily payloads in metallurgy, cement, and automotive plants. Selection turns on load mass, environment, layout geometry, and accumulation needs, not unit price alone.
Roller conveyor systems divide into gravity, motorized-drive, and belt-driven idler types spanning 63–219 mm shell diameters, with CEMA Class E/F bearings standard for mining and palm-oil service. Selection hinges on load, environment, and belt speed, not catalog price.

Belt conveyors carry light-to-medium bulk loads at 5-60 m/min via continuous fabric or rubber belts; chain conveyors move heavy, hot, or abrasive loads via welded/wire-mesh/roller chain. Selection turns on load weight, temperature, cleanliness, incline angle, and maintenance access.

Harmonic drive reducers and planetary reducers cover overlapping servo and robot axis duties but diverge on ratio, backlash, torque density, and footprint. Harmonic units deliver single-stage ratios from 50:1 to 160:1 with near-zero backlash; planetary units span lower ratios with higher continuous
Choose a planetary gearbox by matching torque, ratio, radial/axial load, backlash, and input frame to the driven machine, not by price. Industrial units span 0.09–150 kW, 10–10000+ Nm, ratios 3:1 to 3200:1, and efficiencies above 95%, so mis-sizing is the dominant failure mode.
Slewing bearings buy on four gates: load case (radial/axial/tilt), raceway type (ball vs crossed-roller), gear option (none/internal/external), and IP/grease spec. 2026-07 factory FOB for four-point-contact ball units starts around US$15.50/pc at 1-pc MOQ on Made-in-China.

Disc coupling total cost of ownership hinges on five moveable drivers: torque-class sizing, material (steel vs stainless vs Inconel), API 671 vs AGMA sizing compliance, balance grade, and required misalignment capacity. A 20-year TCO model typically shows purchase at 20-30% of lifecycle cost, mainte

DirectIndustry lists 35 manufacturers and 184 metal conveyor chain products, with China-based suppliers on Alibaba and Made-in-China dominating volume. ISO 606, ISO 1275, and ISO 9001 are the recurring standards cited across listings from Tsubakimoto, 4B Braime, REGINA, and Renold.

Gear coupling sourcing in mid-2026 spans Chinese OEM clusters (Jiangsu/Zhejiang/Chongqing), Indian custom gear shops (Ahmedabad, Bangalore, Mumbai) and US engineering distributors. Key spec gates: torque rating, bore range, AGMA/ISO 6336 alignment, MOQ 1–10 pieces, FOB US$5–921.
Stainless-steel 440C or ceramic-hybrid angular contact bearings with food-grade H1 grease and C-ring or PBR contact-lip seals are the practical F&B workhorses; classic 7200/7300-series chrome-steel units belong in conveyor idlers, not washdown zones.
Pillow block bearings are pre-assembled housings with an insert ball bearing (UC type) or self-aligning ball bearing, designed for light-to-moderate loads on small to medium shafts. Standalone ball bearings are unmounted rolling elements that fit inside a machine and require separate alignment, seal

Pillow block bearings are pre-assembled bearing inserts in one-piece housings, most commonly the UCP200-series ball-bearing type, and they support rotating shafts on conveyors, fans, agricultural, and packaging equipment. Selection is driven by housing shape, locking method, and load class, and they

Linear ball bearings suit high-speed, low-friction, precision applications on hardened shafts, while plain (sliding) linear bearings win on heavy static load, shock absorption, and dusty/washdown environments. Selection hinges on load, speed, precision, environment, and maintenance; cost gap narrows

Linear bearings split into two engineering families: rolling-element (ball and roller) units for high-speed, high-load, precision runs, and plain (bush/sleeve) units for low-friction, contamination-tolerant service. Selection pivots on load rating, stroke, accuracy, lubrication, environment, and lif

Angular contact ball bearings transfer combined radial and single-direction axial loads through a defined contact angle, with 15°, 30°, and 40° as the most common ISO-coded options across 7200/7300 single-row and 3200/3300 double-row series.

Tapered roller bearings use line contact for combined radial + axial load capacity and longer service life, while deep groove ball bearings use point contact for higher speed, lower friction, and primarily radial load support. Selection hinges on load direction, RPM, misalignment tolerance, and cata

Tapered roller bearings are separable, line-contact rolling-element bearings that combine radial and axial load capacity in one unit. Single-row TS types dominate general industrial use, while two- and four-row variants handle heavier radial loads in rolling mills and wind turbines, all standardized
Spherical roller bearings and ball bearings serve different duties: spherical rollers use line contact and self-align to carry heavy radial loads and misalignment, while ball bearings use point contact for high speed and low friction. For shock/heavy radial service choose spherical roller bearings;
Spherical roller bearings (SRBs) are double-row self-aligning radial bearings with bores from 20 mm to 900 mm, offered in cylindrical or tapered bore (1:12 standard, 1:30 for series 240/241) variants. They handle heavy radial loads plus bidirectional axial loads with typical misalignment tolerance a

Spherical roller bearings carry heavy radial plus bidirectional axial loads and self-align for shaft misalignment. Selection hinges on bore type, clearance class, cage, lubrication, seals, and dimensional series matched to load, speed, and environment.

Deep groove ball bearings (DGBBs) carry radial load plus a limited bidirectional axial load, while the broader ball-bearing family spans angular contact, thrust, and self-aligning variants built for higher axial or combined loads. Engineers should pick DGBBs for high-speed, low-to-moderate radial du
Deep groove ball bearing supply runs through global OEM catalogues (Timken, SKF, NSK, Schaeffler/FAG, NTN, Koyo) plus regional distributors, with ISO 15:2017 boundary dimensions covering 3 mm to 400 mm bores. Selection is driven by series (618/619/60/62/63/64), clearance (C2 to C5), and closure (Z,

Single-row deep groove ball bearings are the most common rolling bearing, carrying radial and bidirectional axial loads, with metric series 618, 619, 60, 62, 63 covering bores from 10 to 800 mm across pressed-steel, polyamide, and machined-brass cage options.
Choose a deep groove ball bearing by matching ISO 15:2017 boundary dimensions, dynamic load rating C, and seal/cage variant to radial+axial load, speed, and contamination exposure. Bore 3-400 mm, OD up to 600 mm.

Spring washers deliver low-cost anti-loosening and tension retention under vibration, but the design is highly sensitive to material grade, heat treatment, and split geometry — making supplier qualification the decisive factor in whether they protect or quietly crack a joint.
Spring washer installation succeeds when the washer is oriented with its concave face to the bearing surface, paired with a correctly torqued bolt per DIN 7980 / BS 4464 sizing, and re-checked after vibration cycling.

Spring washers divide into five functional families: Belleville (conical), curved, wave, finger, and split-ring lock washers. Selection is driven by load-deflection curve, material grade (DIN 7980 spring steel, A2/A4 stainless), and standard sizing (DIN 7980, BS 4464, IS 3063).

A taper bush (BTL / Taper-Lock / QD / HE) is a split, tapered sleeve that locks a hub to a shaft via axial screw force; correct install runs clean → insert → hand-start screws → alternately torque to spec (e.g. 1008 = 55 lb·ft) → re-tap the large end on 3535+ sizes → fill unoccupied holes with greas
Field-tested shaft collar installation hinges on matching collar style (solid, one-piece split, two-piece split) to shaft tolerance, torque load, and axial-travel needs. Correct torque, bore-to-shaft fit, and DIN 705-grade dimensional checks prevent 80% of premature field failures.
Shaft collars are classified into set-screw, clamp (one-piece), and split (one- and two-piece) styles, with materials spanning zinc-plated steel, black-oxide steel, 303/316 stainless, and anodized aluminium, sized from 6 mm to 75 mm bore.
Shaft keys transmit torque through positive mechanical locking between a shaft and hub, with parallel keys (GB/T 1095) and Woodruff keys (GB/T 1096) dominating general industrial use. Selection hinges on torque, shaft diameter, keyway stress concentration, and assembly access rather than cost alone.
Shaft key installation hinges on three measurable checks: key-seat tolerance to ISO 773 / ISO R773, parallel gib-head clearance in the keyway, and interference between key and keyseat. Skipping any of these is the root cause of almost every keyway-side field failure logged by maintenance crews.

Shaft keys are metal inserts that lock rotating hubs to shafts via matching keyseat and keyway slots. Parallel, Woodruff, taper, gib-head, feather, spline and round are the seven families engineers spec against ISO 2491 / DIN 6885 / ANSI B17.1, with selection driven by torque, hub axial travel, and

Retaining rings (snap rings, circlips) eliminate the need for threaded fasteners, shoulders, or machined grooves wider than the ring itself, cutting assembly cost and axial envelope by 30–60% versus shoulder screws. They suit high-volume, low-vibration shaft/housing retention but are wrong for high-
Retaining ring installation relies on matching ring style (external, internal, spiral, snap) to groove geometry, using correct pliers or applicator tooling, and verifying groove dimensions against DIN 471/472 or ANSI B27.7 before axial loading. Common failure modes stem from over-spreading, undersiz

A locking assembly TCO model driven by shaft fit class, surface finish, and torque rating typically triples purchase price over a 10-year horizon, with installation labor, unplanned downtime, and replacement cycles dominating. Buyers who skip lifecycle modeling underestimate true cost by 2-4x.

Lock nut total cost of ownership is driven by five lifecycle stages—material, install labor, retorque, replacement, and downtime—and the cheapest unit price rarely wins. Specification choices on material grade, thread class, and locking mechanism shift 10-year cost by 2–4×.

Lock nuts add a second friction interface to a bolted joint to resist self-loosening from vibration and shock, but they cost more, add height, lengthen assembly time, and can gall or crack the parent thread if over-torqued.

Lock nuts — also called locknuts, stop nuts, or self-locking nuts — are specialized threaded fasteners built to resist loosening under vibration, shock, or thermal cycling. Six widely stocked families cover most industrial needs: FLEXLOC all-metal, nylon-insert, 12-point, aerospace MS/AN, barrel, an

Belt tensioner TCO is dominated by the wear-driven replacement cycle, drive-side downtime exposure, and matched-belt compatibility, not the unit purchase price. Across a typical 5–8 year service window, indirect cost components (unplanned stoppages, belt-edge damage, labour for re-tension) routinely
A correct belt tensioner installation on a serpentine or V-ribbed belt drive follows four checks: match OE part number and rib count, set deflection to spec, torque the centre bolt to the OEM Nm value, then re-tension after 50–100 km or one heat cycle.
V-ribbed belt installation on modern European engines requires matched tensioner, deflection/guide pulley, and rib-section PJ/PK/PL belt per OEM cross-reference. 2026 aftermarket data shows 6-rib PK units at 69 mm OD, 37-248 g pulleys, and OE part numbers from BMW 11 28 7 800 562 to MERCEDES-BENZ 27
V-ribbed belts are classified by rib-section profile — PH, PJ, PK, PL — with rib pitch from 1.6 mm to 4.7 mm, belt thickness 3–10 mm, and 3 to 160 ribs. Selection depends on driven-unit load, pulley diameter, and OEM fitment data such as MERCEDES-BENZ 6512000670 and BMW 11282248169.

Flat belt TCO is dominated by belt replacement, drive energy, and tensioner maintenance — not by purchase price. A published TCO framework typically shows purchase price contributing under one-fifth of lifecycle cost, with operations and maintenance exceeding half across the asset's service life.

Flat belt installation on a troughed or slider-bed conveyor hinges on three mechanical facts: pulley parallelism under 0.5° per meter, a static belt tension window that keeps the carcass above the rated working load, and pulley lagging that raises the friction coefficient above 0.35. Get any one of

Conveyor chain delivers high load capacity, long life, and stable performance under heavy-duty, high-temperature, or oily conditions, but trades noise, speed limits, and maintenance overhead against belt or roller alternatives. Best fit for pallet lines, automotive assembly, and bottling; skip it fo
Conveyor chain selection hinges on matching pitch series (X348/X458/X678 drop-forged, WR/WH welded steel, 40/50/60 double-pitch roller) to load, environment, and attachment layout. Standards BS 4116-4:1992 and ISO 9001 govern British-series chain dimensions and manufacturer quality systems. Decision

Silent chain TCO hinges on four cost drivers: acquisition price (25-35%), lubrication and energy (20-30%), downtime (15-25%), and disposal. Selection on pitch and tensile grade alone typically overstates savings by 12-18% versus full lifecycle modelling. Lifespan extends 2-4x when matched correctly

Silent chain (toothed chain) is a low-noise, high-speed, heavy-load transmission built from staggered toothed plates joined by pins, bushes, or rollers. Four construction variants — double-pin, double-swing, double-pitch, and laser-welded pin-end — cover most automotive, industrial-pump, and machine
Chain and gear sprockets deliver high efficiency (typically 95–98%), compact envelope, and a 5–10 year service life on enclosed drives, but they add radial load, require lubrication, and need alignment within 0.05–0.15 mm/m for quiet operation.

Sprocket installation hinges on matching pitch, tooth count, and bore tolerance to the chain and shaft before any axial fixation. Specs to verify: BS/ASA chain pitch (04B-32B or ASA35-100), bore to H7, keyway to JS9, and correct rotation direction stamped on the hub. Misalignment beyond 1° between d

A V-belt's purchase price covers roughly 10–30% of its lifetime cost; the remaining 70–90% is consumed by premature replacement labor, unplanned downtime, matched-pulley wear, and energy losses from slip and bending. Real TCO control means sizing the drive, matching the belt section to the pulley gr
V-belt drives use 30°–40° trapezoidal grooves to multiply friction and transmit high power across short centers, but the same wedging geometry that grips the pulley rules out long spans, high speeds above ~50 m/s, and any application that needs zero slip. They are the workhorse of industrial drives

Timing-belt TCO over a 5-year service window is dominated by replacement-belt inventory, downtime labour, and tensioner/pulley wear, not by the belt's sticker price. Buy on matched tooth profile, pitch, compound, and verified service hours per ISO 5293 / ISO 13050, then plan PM intervals against the
Timing belts deliver up to 98% mechanical efficiency with positive slip-proof tooth engagement, but pay for it with higher cost, no overload protection, and sensitivity to oil and heat that ages the rubber. They are the right pick when synchronous, low-maintenance, high-speed motion is needed; they

Industrial timing-belt installation hinges on four mechanical checkpoints: lock-out/tag-out, no-pry removal, pulley cleaning, and alignment under 1/4° or 1/16 in/ft. Aftermarket deflection/guide pulleys fit 60-68 mm OD, 24-38 mm width ranges. Verify tooth profile, length, and tensioner before torque

Timing belts are classified by tooth profile (trapezoidal HTD/STD, curvilinear RPP, and polyurethane steel-core), by pitch family (metric 3M/5M/8M vs imperial XL/L/H), and by application load band. Selecting the right type depends on torque, speed, environmental exposure, and matching to a compatibl

Roller chain TCO runs 3-5x the purchase price over a 5-year life, driven mainly by lubrication spend, replacement chains, and unplanned line stoppages. Use this cost-driver map to size the real budget per drive.
A roller chain transmits power through meshing of pins, bushings, and rollers with sprocket teeth, with a 95-98% mechanical efficiency in well-lubricated ISO 606 single-strand drives. Main trade-off: high power density at low cost versus stretch wear, lubrication demand, and noise above ~10 m/s chai

Roller chain installation on ANSI #40–#160 drives follows a 4-step process: verify shaft alignment within 1°–2°, set mid-span deflection to 2%–3% of span, match sprocket tooth count to speed ratio, and pre-load tension. Wrong sag or misalignment causes 60% of premature failures per field data.

Roller chain types map cleanly onto three decision axes: standard (ANSI B29.1 vs ISO 606/DIN 8187/BS 228 vs GB/T 1243), duty class (standard short-pitch, heavy/extra-heavy, double-pitch), and environment (stainless, nickel/zinc/Dacromet-coated, O-ring/X-ring sealed). Match chain size and series to s
Industrial shock absorber TCO spans acquisition, installation, energy, preventive maintenance, and end-of-life disposal over 5-10 year service windows. Hydraulic, gas-charged, and pneumatic-damper designs each carry distinct cost drivers — material grade, damping fluid, seal life, and certification

Industrial shock absorbers are sized by per-cycle energy (E=J), impact velocity (m/s), and effective mass (kg), with installation torque, stroke usage, and ambient envelope deciding real-world fit. Standard adjustable hydraulic units cover 0.3–5.0 m/s, low-velocity models 0.08–1.3 m/s, -10 to 80 °C

Industrial shock absorbers split into hydraulic, pneumatic, rubber/elastomeric, and adjustable damping families, each matched to energy, cycle rate, and environment. Selection hinges on kinetic energy per cycle, peak force, stroke, and operating temperature rather than generic duty labels. Catalog S

Fluid coupling TCO hinges on slip-driven power loss, working-fluid and seal service, and overload-event frequency; acquisition is roughly 20-30% of 10-year lifecycle cost.

Fluid couplings transmit torque hydrodynamically with no mechanical contact, delivering soft starts, overload protection, and shock-load damping, but they suffer inherent slip of 3–15% and torque capacity that collapses to zero at synchronous speed. Specify them for high-inertia starts on conveyors,

Fluid coupling installation hinges on shaft alignment within 0.1–0.2 mm, a constant-fill charge verified by plug dipstick, and a delay chamber sized to the driven load. This guide lays out the mechanical checks, fluid-fill rules, and start-up tests a process engineer needs to commission a hydrodynam

Fluid couplings are hydrodynamic power-transmission devices classified into constant-fill, variable-fill, and delay (soft-start) chambers, distinguished by torque capacity, slip behaviour, and whether a working fluid is exchanged at runtime. This article maps the three primary types against app

A jaw coupling's purchase price typically represents 15-25% of its 20-year total cost of ownership; the remaining 75-85% is dominated by downtime losses, elastomer replacement, alignment labor, and energy dissipated as hysteresis heat.
Jaw couplings cover 1.2 Nm to 161,003 Nm across Lovejoy, Weasler, ALBERT and BEA Ingranaggi lines, and installation depends on hub fit, spider elastomer, and angular/parallel misalignment limits. Field guide.

Jaw couplings are classified by elastomer hardness (Shore A), hub material, and assembly style, spanning 0.7 Nm miniatures to 130,000 Nm backlash-free spacer designs. Selection hinges on torque, speed, misalignment window, and electrical-isolation need.

Disc couplings transmit torque through a stacked stainless-steel or composite diaphragm pack, delivering zero backlash and high torsional stiffness in a compact envelope, but they offer limited misalignment capacity and shock-load damping. They are specified for precision servo, pump, and turbomachi

Disc coupling installation demands controlled bolt torque, tight angular/axial alignment limits, and API 610 spacer compliance to avoid premature disc-pack fatigue and backlash drift.

Disc couplings are torsionally rigid flexible couplings classified by disc-pack configuration (single, double, floating-shaft), bolt count (4/6/8), and hub/spacer style, with torque envelopes spanning ~35 Nm to 176,000 Nm and speed ceilings from 2,300 to 22,500 rpm across current OEM catalogs. API 6
Clutch and brake TCO is dominated by energy, wear-part replacement, and downtime, often exceeding the unit purchase price 5-10x over a 10-year service life. Specifying torque margin, duty cycle, and lubrication intervals up front reduces the lifetime cost per operating hour significantly.
Industrial clutch and brake installation hinges on three checkpoints: shaft alignment within 0.05-0.10 mm, runout under 0.05 mm TIR, and an air gap of 0.4-0.8 mm on electromagnetic units. Skip them and you trade a four-hour commissioning for a four-week teardown.
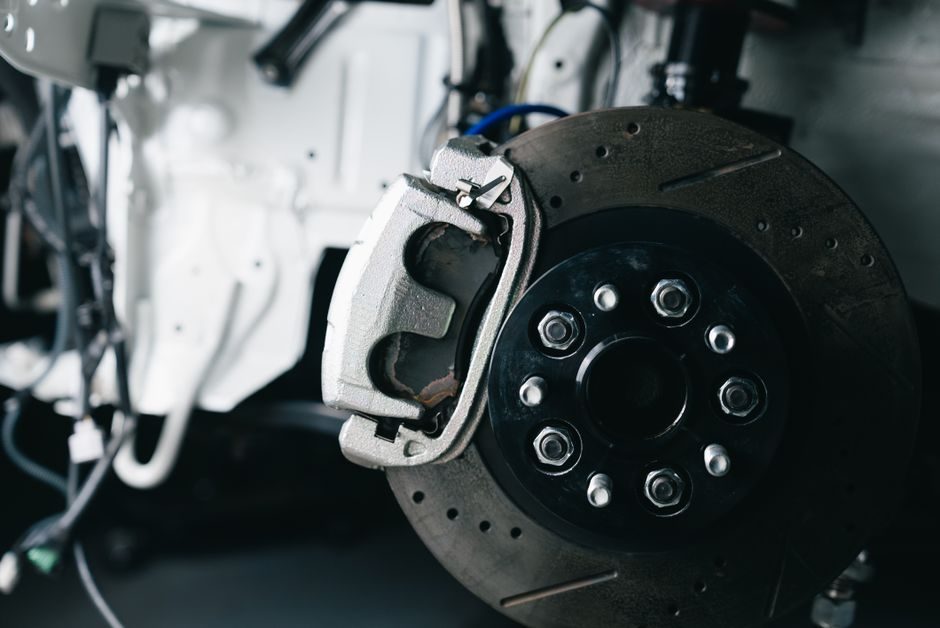
Industrial clutches and brakes split into electromagnetic, pneumatic, hydraulic, and mechanical-spring families, each picked by actuation medium, torque density, and cycle rate. Warner Electric's TCS-200 series and Hawers' HACB piston-type line, both catalogued in 2025-2026, illustrate the current 2

Flexible couplings such as elastomer, jaw, gear, grid, bellows and disc types absorb torsional shock and compensate parallel, angular and axial misalignment of 0.1–3 mm typical during installation. Correct alignment, key/shaft-key fit and torque capacity verification against service load decide a 20

Shaft couplings fall into two top-level families — rigid and flexible — with flexible further split into elastomeric, disc/bellows, gear, and universal-joint subtypes. Selection is driven by torque, speed, misalignment budget, and environment; disc and gear couplings dominate high-torque industrial
Linear module total cost of ownership is dominated by 5-10 year maintenance, lubrication, and downtime exposure, not the unit price. Spec steel-bodied modules with self-lubricating 30,000 km service intervals, IP-sealed strips, and built-in linear rails to keep TCO defensible.
Linear modules are classified by drive type (ball screw, belt, linear motor), guideway (ball rail, cam roller, crossed roller), and axis count (single, XY, XYZ). Selection hinges on stroke, load, speed, and repeatability, with light-duty MGN-size modules serving pick-and-place and heavy-duty MKK/MLR
Crossed roller guide TCO is dominated by unplanned downtime, lubrication cadence, and preload drift, not the catalog rail price. On an NG-series profiled guideway rated 850–1,800 N over 50–400 mm of rail length, lifecycle cost typically runs 3–7× the purchase figure once re-lubrication, alignment, a
Crossed roller guides deliver high rigidity and load capacity in compact linear-motion envelopes but trade speed, cost, and contamination tolerance against recirculating ball guides. Selection hinges on load-to-size ratio, precision envelope, and duty cycle.
Crossed roller guide installation hinges on a flat datum within 0.02 mm across the mounting footprint, preload set to 0-3% of dynamic load, and torque-stage lubrication. Ewellix LW/LWRE and Rosa Sistemi NG series bracket the spec envelope at 999-22,440 N load, 1 µm precision, and 120 °C ceiling

Ball spline TCO is dominated by 5-10x hidden lifecycle costs beyond purchase, with lubrication regime, seal integrity, and stroke-aligned load rating driving 80%+ of total spend over a 10-year horizon.
Lead screw TCO is driven by initial unit cost, lubrication regime, duty cycle, and replacement interval over a 5-10 year horizon. Acquisition typically represents only 15-30% of lifetime spend.
A correctly installed lead screw assembly pairs a right-hand threaded shaft with a matched nut, mounts the screw between two bearing-supported ends with parallelism under 0.02 mm/m, and verifies the kinematic ratio ωS = (2π/L)·vN against travel.

Lead screws convert rotary motion to linear thrust via a threaded shaft and nut, classified by thread form (Acme, square, trapezoidal, buttress), drive element (sliding vs. rolling), and self-locking behaviour. Sliding (sliding-contact) Acme and trapezoidal units dominate general industrial use; bal

Linear actuator TCO is dominated by motor and ball-screw lifecycle cost, with 5-year ownership typically running 2.5-4x unit price once energy, duty-cycle, and IP-rated enclosure factors are priced in.

Linear actuators deliver straight-line force with stroke repeatability typically ±0.05 mm and ball-screw service life up to 10,000 km, but backlash, duty-cycle limits, and seal wear are the trade-offs engineers must price into every build.
Linear actuators convert rotary, hydraulic, pneumatic or piezo input into controlled straight-line motion and split into six drive classes: electric, hydraulic, pneumatic, mechanical, piezo, and electromagnetic. Selection hinges on force (N), stroke (mm), speed (mm/s), duty cycle, environment, and f
Ball screws convert rotary motion to linear motion with 90%+ mechanical efficiency and lead accuracy down to ±0.0005 in/ft on precision-ground units, but cost 3-10× more than lead screws, require strict contamination control, and lose preload under shock load. Choose ground ball screws for CNC axes;
Ball screw installation hinges on four gates: concentric alignment to support bearings, preload-matched angular-contact bearing blocks, lubrication interval by duty cycle, and end-fixity consistent with manufacturer thrust specs. Pitches span 0.5 mm miniature to 16 mm heavy-duty, with position

Ball screws are classified by manufacturing process (precision-ground vs rolled), ball-circulation method (end-cap, return-pipe, deflector), and ISO accuracy grade C0–C10, with each axis driving cost, lead-time, and duty envelope.

Linear guide TCO spans purchase, lubrication, energy, downtime, and disposal over a 5–10 year service window. Procurement cost is typically 15–30% of lifetime spend; the remainder hides in lubrication, contamination-driven wear, and unplanned stops. This article breaks the cost stack and ranks the p

Linear guides deliver sub-micron positioning accuracy and 10+ year service life when correctly specified to load and rigidity class, but cost 3-8x more than plain bearings and demand strict contamination control.

Linear guide installation: secure rail-to-bed flatness at 5 µm, tighten M3–M8 mounting screws to 1.0–29.4 N·m on SCM sockets, and align the second rail to a master datum using a straightedge and dial indicator within 10–30 µm/200 mm parallelism.

Slewing drive TCO over a 10–15 year service life is dominated by the initial gearbox-and-bearing cost, annual torque-motor energy draw, and seal/gear-lubricant replacement cycles. A spec-first model that prices acquisition against the dominant opex line — grease, energy, and crane-lift downtime — ty
Slewing drives are classified by gear mesh type, drive configuration, and output torque range, with worm-gear single-envelope units dominating solar tracking and worm-planetary dual-stage units covering crane and aerial-work-platform duty cycles up to 400 kNm.
A variable speed drive (VSD) cuts total cost of ownership by trimming energy spend, the dominant lifetime cost driver, but only when load profile and duty cycle justify the inverter premium. Quantify purchase, energy, heat, maintenance, and disposal before specifying a VSD over a fixed-speed unit.

Variable speed drives (VSDs, also called VFDs) cut AC motor energy use by matching speed to load on fans, pumps, and conveyors, but they add harmonic distortion, common-mode voltage, and higher upfront cost that engineers must spec around. Use a VSD on variable-torque loads; skip it on constant-spee

Variable Speed Drive installation follows a 4-parameter commissioning baseline (motor rated current, RPM, voltage, power), with low-voltage units spanning 0.25–132 kW, IP20/NEMA 1 enclosures, and dual-channel STO to SIL3/PLe under EN/IEC 61800-5-2.

A variable speed drive (VSD) is a power-conversion + motor-control unit classified by phase (single/three-phase), control mode (V/F, vector, direct torque), topology (two-level vs multi-level), and load fit, with industrial ratings spanning 0.4 kW to 2,800 kW across current DirectIndustry listings [

A helical gear reducer's true 10-year cost is dominated by energy loss and unplanned downtime, not the purchase invoice. Procurement teams that model only first-cost typically underestimate lifetime spend by 2-4× once efficiency, lubricant service, and bearing replacement are included.
Helical gear reducers deliver 95–98% single-stage efficiency and high torque density, making them the default for parallel-shaft drives above 5 kNm; the trade-off is thrust load, oil-leak risk, and higher cost-per-kW than worm units.
Helical gear reducer installation hinges on rigid foundation, precise shaft alignment under 0.05 mm, correct mounting bolt grade, and oil-bath commissioning. Backlash on precision units runs 0.02-0.12 deg, ratios 5-220:1.

Helical gear reducers are classified by shaft orientation (coaxial, parallel-shaft, right-angle), stage count, mounting, and torque class, with the 2026 product set spanning 10 Nm compact modules to 10 kNm heavy-duty units. Selection hinges on torque, ratio, duty cycle, and footprint, not brand.
An RV reducer's true 10-year cost is dominated by downtime, lubrication cycles, and backlash-driven yield loss rather than the unit sticker price, so a spec-first TCO model should weight MTBF, grease interval, and torque margin above acquisition. Use this guide to map cost drivers against RV, harmon

RV reducer installation hinges on bolt-grade selection, shaft-seating concentricity, oil-fill protocol, and run-in verification. Use 12.9-grade bolts for servo-to-reducer and reducer-to-housing joints, follow a staged torque sequence, and confirm backlash before load.
Harmonic Drive reducer TCO runs 2–4× the unit price over a 10-year life, driven by grease change intervals, single-tooth-count mismatch penalties, and flexspline replacement. Acquisition is ~25–35% of lifetime spend; lubrication, energy losses, and downtime dominate the rest.
Harmonic-drive reducers deliver zero backlash, ratios from 30:1 to 160:1, and torque density up to 545 Nm/kg, but trade that against limited shock load capacity and a three-component design that's intolerant of misalignment.

Cycloidal reducers deliver single-stage ratios up to 1:87 at 90-97% efficiency with two-tooth meshing, but cap high-speed shaft input at roughly 1500-1800 rpm and demand tight GCr15 bearing-steel tolerances that push cost and maintenance complexity above helical alternatives.
RV-E cycloidal reducers ship grease-free and need 85% fill of special ZKRV grease on a 2000-hour first-change interval, with backlash under 1 arc.min across 200 Nm-5 kNm. Correct shim, O-ring and coupling alignment prevent the early failures seen in field service.

Cycloidal reducers split into two main families: standard cycloidal-pinwheel units (0.04-132 kW, ratios 1/6 to 1/446571 across 1-3 stages) for general drive duty, and precision RV cycloidal gearboxes (ratios 41-7569, two-stage closed differential) for robotics. Selection hinges on output form, backl
Industrial gear TCO over a 10-year horizon is driven by energy loss, lubricant and seal service, and unplanned downtime, with purchase price typically under 30% of lifecycle spend. Selection requires ranking gears on efficiency class, L10 life, and mean-time-between-failure before quoting.
Industrial gears — including spur, helical, bevel, worm, and planetary families — deliver high torque density and long service life, but each type carries distinct noise, efficiency, lubrication, and backlash trade-offs that drive selection. Spec-driven choice between material, geometry, and lubrica
Industrial gear installation hinges on five prep gates: PPE and work-area clearance, mounting arrangement (straddle vs overhung), shaft alignment within 0.05–0.10 mm, contact-pattern and backlash verification, and oil-type match to ambient. Skipping any gate is the dominant cause of premature bearin

Industrial gears are classified by shaft-axis geometry into parallel, intersecting, and skew types, with spur, helical, bevel, and worm variants dominating industrial gearbox design and sourcing decisions worldwide.

Worm gear reducer total cost of ownership is dominated by energy losses, lubricant spend, and seal replacement rather than purchase price. Single-stage worm units typically run 30-60% efficient versus 90-98% for helical or planetary units, so over a 10-year duty cycle energy can dwarf a 3-5x higher-

Worm gear reducers are classified by shaft orientation (right-angle vs coaxial), shaft configuration (solid vs hollow), housing material (aluminium, cast iron, stainless), and torque band, typically from 5 Nm to over 10 kNm per stage. Selection pivots on ratio, self-locking, efficiency (50-90%), and
Planetary reducer TCO is dominated by efficiency-driven energy loss and unplanned downtime, not purchase price. A 2-3% efficiency gap across a 20,000-hour service life shifts five-year spend by 8-15% on most industrial drives.

Planetary reducers deliver 95–98% stage efficiency and coaxial torque density unmatched by worm or helical units, but cost more, run hotter in over-ratio stages, and are limited on input speeds above ~8,000 rpm. They are the default pick for servo-driven precision motion, not for shock-loaded or low

Planetary reducer installation hinges on shaft alignment within ≤0.05 mm, fastener torque to OEM values, and lubricant grade matched to ambient. Mounting style (flange, foot, hollow-shaft) and backlash class drive acceptance thresholds.

Planetary reducers are classified by gear geometry (spur vs helical), stage count, output form (solid shaft, hollow shaft, right-angle, flange), and precision tier; selection maps onto backlash (≤15 arcmin typical for precision), ratio range (3:1–200:1), and torque class (6–32 N·m for compact precis

Industrial gearbox installation hinges on four spec-driven checkpoints: foundation flatness per DIN ISO 2768-2, shaft tolerances of ISO 8015 H7/h6, interference-fit heating to 250–300°F, and pre-commissioning alignment plus oil verification. Skip any one and bearing life drops by an order of magnitu

A 5-7 year slewing-bearing TCO is dominated by five cost levers — initial purchase, lubrication regime, mounting/alignment labor, unplanned downtime, and end-of-life scrap — and a structured cost stack can move lifecycle spend by 20-40% versus a purchase-price-only comparison.

Slewing bearings are large-diameter rolling bearings that handle combined axial, radial, and moment loads in one raceway, classified by rolling element into single-row four-point contact ball, double-row ball, cross-roller, and three-row roller types. Selection is driven by load mix, diameter range
Slewing ring bearing TCO is driven by five cost levers: initial purchase (bearing type and diameter), lubrication regime, mounting/alignment labor, downtime, and end-of-life rebuild. Over a 5-7 year window, purchase typically represents 20-30% of total spend, with maintenance, downtime and energy lo
Slewing ring bearing installation hinges on bolt torque control, raceway soft-zone alignment to the load vector, and verified gear-tooth backlash. A 1,310 mm internal-toothed SBI SLIR20 four-point contact ball unit illustrates typical industrial scale, with 50Mn or 42CrMo raceways standard on Chines
Slewing ring bearings split into four structural families — single-row ball, double-row ball, crossed-roller, and triple-row roller — selected by load mix (axial, radial, overturning moment) and duty cycle. Gear options (none / internal / external) are layered on top, and light-section flange varian
Ceramic bearing TCO is dominated by purchase price, lubricant/energy use, downtime loss, and disposal, not just unit cost. Lifecycle math typically recovers the 3-10x steel-bearing price premium within 2-4 years in high-RPM or corrosive service.
Silicon nitride ceramic bearings trade higher upfront cost and brittleness for lower rolling resistance, hardness near 75-80 HRC equivalent, corrosion immunity, and longer service life versus standard steel bearings. Selection hinges on speed, load, environment, and total cost of ownership, not head
Ceramic bearings split into three structural classes — full-ceramic, hybrid, and ceramic-roller — built from Si3N4, ZrO2, SSiC, or Al2O3, with selection driven by load, speed, corrosion and electrical isolation needs per current OEM catalogues.

Spherical plain bearing TCO hinges on five cost drivers — material grade, lubrication regime, load rating, mounting/alignment work, and replacement frequency — with the purchase price typically 20–40% of lifetime cost in heavy industrial duty cycles. Lubricated steel/steel, self-lubricating PTFE-lin

Spherical plain bearings accept misalignment up to roughly 30° while carrying combined radial and axial loads, but their sliding contact raises friction and limits speed to typically under 300 rpm. Maintenance-free PTFE-lined steel/steel pairs (e.g. FLURO GE..FW) suit slow pivots; self-lubricating f

Spherical plain bearing installation follows three sequenced stages — receiving inspection, press-fit mounting, and post-fit lubrication verification — with bore range 5 mm to 600 mm and DIN ISO 12240-1 dimensional conformance governing series K PTFE-lined parts. Selection between through-hardened s

Spherical plain bearings divide into radial, angular-contact, thrust, and rod-end variants, built to DIN ISO 12240-1/-2 in steel/steel, stainless/PTFE, and coated metal-on-metal tribo-pairs from 5 mm to 600 mm bore.
A pillow block bearing's true 10-year cost is dominated by relubrication labor, downtime, and replacement insert swaps — not the housing's sticker price. This TCO analysis maps the cost drivers, the housing-material trade-offs, and the spec checkpoints a process engineer should use before signing a
Pillow block bearings pair a self-aligning insert with a cast or pressed housing, delivering low-cost shaft support for conveyors, fans, and farm machinery. The trade-off is limited speed, load, and misalignment tolerance compared with flange, take-up, or cartridge units.
Pillow block bearing installation in 2026 centres on set-screw UCP/UCF/UCFL insert fits with cast-iron housings, DIN ISO 12240 series geometry, and 41,000 ft² lab-validated service-life data for dry-running polymer units.
Pillow block bearings are mounted bearing units pairing an insert (typically a self-aligning ball bearing) with a cast or pressed-steel housing; classified by housing shape (P/F/FC/FL/T), insert type, material, and bore series UCP201–UCP215.
Tapered roller bearing TCO is dominated by lubrication, contamination control, and alignment quality, not unit price; full lifecycle cost typically runs 3–10× initial purchase over 5–10 years in industrial service.

Tapered roller bearings handle combined radial and axial loads on a single shaft but require paired or adjusted mounting, run hotter at high speed, and lose efficiency under pure radial misalignment. Use them for heavy-duty gearboxes, wheel hubs, and rolling mills; avoid them where strict misalignme
Tapered roller bearing installation hinges on matched bore clearance, controlled cold-mount interference, and verified endplay of 0.05–0.13 mm. Misaligned cups and over-driven sleeves remain the dominant failure modes on single-row units up to 1,270 mm bore.

Tapered roller bearings are classified by row count (single, double, four-row), load direction (radial, thrust, combined), and geometry into types including TSF, TDI, TDO, TNA, and 30000-series metric designs. Selection hinges on combined radial+axial load, bore range 10–220 mm, and operating enviro
Self-aligning ball bearings compensate 1.5°–3° of static misalignment via a spherical outer raceway, but trade load capacity and speed for that forgiveness. Specify them when shaft deflection or mounting error dominates; avoid them in heavy radial or high-speed duty where cylindrical or tapered bear
Self-aligning bearings tolerate 1.5°–3° of static shaft misalignment via a two-row ball path on a spherical outer race; correct install hinges on shaft tolerance, housing-seat geometry, lock-pin orientation, and lubricant fill, per current OEM guidance.

Self-aligning bearings split into two principal rolling-element families — self-aligning ball bearings and spherical roller bearings — plus plain Cu-Be/CRES self-aligning sphericals rated -65°F to +350°F under SAE AS81936A-2006. Selection turns on misalignment tolerance, load profile, and housing ma
Angular contact bearing TCO hinges on lubricant interval, cage material, and alignment accuracy: over a 10-year duty cycle, recurring cost (downtime, grease, energy) typically exceeds purchase price 3-5x. Pumping losses in grease-lubricated 40° contact-angle units above 8,000 rpm drive 2-4% motor-si

Angular contact ball bearings (ACBB) carry combined radial and axial loads via a 15°-40° contact line, deliver higher rigidity than deep-groove types, but trade speed, misalignment tolerance, and seal simplicity. They are the default for machine-tool spindles, pumps, and gearboxes; they are wrong fo

Angular contact bearings are rolling-element bearings whose raceway contact line is offset from the radial plane at a defined nominal angle (typically 15°, 25°, or 40°), letting them carry combined radial + axial load in a single direction. The dominant types in 2026 production are single-row 70000

Linear bearing TCO is dominated by lubrication, contamination exposure, and stroke cycle count, not the unit price; a properly specced linear guide or linear module typically returns 3-5x its purchase cost in avoided downtime over a 10-year service window.

Linear bearings deliver low friction, high rigidity, and repeatable motion under loads ranging from a few newtons to over 100 kN, but trade off speed, contamination sensitivity, and noise versus plain bushings. The right pick depends on load, stroke, accuracy, and environment.
Linear bearing installation follows a five-step spec map: confirm load class and rail width, square the rail within 0.02 mm/m, torque carriage bolts to grade, lubricate per raceway, then run a no-load break-in. Match the bearing type — recirculating ball, plain, or crossed roller — to duty cycle bef

Linear bearings split into two main families — rolling-element types (ball, crossed-roller, needle, LM guide) and plain/sleeve types (self-lubricating bushing, PTFE-lined) — with selection driven by load, stiffness, stroke, contamination, and lubrication regime rather than a single universal winner.
Thrust bearing TCO over a 5-10 year service window is dominated by lubricant, downtime, and energy losses — not the unit price. Map purchase, install, lubrication, energy, and failure-cost drivers before specifying type or material.
Thrust bearings carry pure axial load along the shaft axis using rolling-element or fluid-film contact. Selection hinges on load magnitude, speed (DN), alignment tolerance, and lubrication regime; misalignment, shock load, and high radial load are disqualifying conditions.
Thrust bearing installation is governed by bearing type and load path: tilting-pad thrust units handle >4 MPa at 160 m/s sliding speed per MIBA, while hydro-generator units follow SL 668-2014 process rules. The install decision tree is fit type, alignment tolerance, lubrication, and accept

Thrust bearings support axial loads and split into rolling-element types (ball, cylindrical roller, tapered roller, spherical roller, needle) and hydrodynamic fluid-film types (tilting-pad, tapered-land, plain). Selection is driven by load magnitude, speed, misalignment tolerance, and required life,
Roller bearing TCO is dominated by unplanned downtime and lubrication regime, not purchase price; a 5-year cost stack typically allocates 3-10% to acquisition, 60-80% to operations and lost production, and 10-25% to maintenance, with ISO 15243 failure-mode classification as the engineering baseline.
Roller bearing installation succeeds when shaft and housing tolerance classes match the bearing specs, mounting force is applied only to the ring being press-fit, and pre-load is set against a measurable torque or starting-current value rather than feel.

Roller bearings are classified by rolling element geometry into cylindrical, needle, tapered, spherical, and crossed-roller families, each handling different radial/axial load ratios, speed limits, and misalignment tolerance. Selection hinges on load direction, RPM, mounting style, and whether the a
Deep-groove ball bearings deliver low friction, very high speed capability, and dependable overload tolerance, but pay for it with noise at speed, dirt sensitivity, and limited shock/axial load capacity versus cylindrical or tapered roller types. Specify them where radial load dominates, speeds exce

Ball bearings classify by load direction (radial, thrust, angular contact), rolling-element geometry, and raceway conformity; deep-groove, angular-contact, self-aligning, and thrust types cover ~90% of industrial demand. Selection pivots on load vector, speed, misalignment tolerance, and ma

Linear actuators convert rotary, pneumatic, hydraulic, piezo, or electromagnetic input into controlled straight-line motion and are classified into six drive classes. Selection hinges on force, stroke, speed, accuracy, and environment, with electric and pneumatic units dominating 12V/24V mobile use

Spring washer sourcing in 2026 is dominated by Asian B2B platforms listing 500+ M3 split-lockwasher SKUs from 100+ Chinese suppliers, with hex-bolt/nut/spring-washer kit pricing at US$0.23-23.00 per 1,000-piece MOQ and MOQs typically 1,000-10,000 pieces.
Spring washer selection hinges on four numbers: required load, work height, bore/shaft geometry, and material. DIN 2093 disc springs cover 8–71 mm OD and 0.3–2 mm thickness; wave springs follow a stricter 2–20 turns rule with stress capped at 100% static, 80% dynamic.

Pick a spring washer by matching its profile to the joint duty: split-lock or wave for light-vibration bolted joints, conical (Belleville) for high-load pre-load retention, and disc-spring stacks where space is tight and load must be tunable. Verify material/hardness, standard (DIN 127, DIN 6796, DI

A taper bush is a split, tapered locking sleeve that mounts a pulley, sprocket, or coupling to a shaft without keyways. Selection hinges on bore range, bushing series (1008-5050), shaft tolerance h6/h7, and duty cycle.

Shaft collar sourcing in 2026 splits into two clear channels: US/EU stock-and-spec specialists (Ruland, Climax, Stafford, Huco) for traceable inch/metric parts, and Chinese DIN 705 / split-collar OEM lines out of Ningbo, Zhejiang where 2-piece collars land near US $1/piece FOB. Material grade, bore
Shaft collar sizing and selection in 2026: bore to shaft fit (g6/h7), one-piece vs split (1- vs 2-piece) construction, material pick (steel, 303/304/316 SS, aluminum), set-screw torque, and load case drive the call. Match collar to the job: clamp vs stop vs spacer vs mounting platform.

Stainless steel 316 two-piece clamp-style shaft collars dominate chemical-processing duty, with 1-1/2 in to 3 in bore sizes being the most specified range. For corrosive CIP washdown or acidic media exposure, specify 316 stainless with electropolish; mild dry duty tolerates zinc-plated carbon steel.

Choose a shaft collar by matching style (solid, one-piece clamp, two-piece clamp, split) to shaft finish, torque, and rework needs. Stainless 304 slit collars ship same-day in 6-50 mm bore; two-piece clamp collars handle higher torque with full shaft contact.

Made-in-China lists 2,000+ shaft manufacturers and 6,000+ products as of April 2026, with shaft-key material suppliers on Alibaba showing tier-1 listings at US$1–10 per piece on 10-piece MOQs. Cimo Transmission (Zhejiang) and Changzhou Chengli Precision Equipment anchor the keyless-locking and air-s

Shaft key sizing and selection in 2026 still rides on square/parallel/retained-key geometry, ISO metric shaft tolerances, and the half-key convention in ISO 21940-32:2012 for rotor balance. Use this guide to match key type to load, hub travel, and assembly method.
For data-center cooling fans, pumps and CRAC blower shafts, the most reliable shaft-key choice is an ANSI B17.1 parallel square or rectangular key in 4140 or 316 stainless steel, sized per the standard shaft-diameter table (e.g. W=3/8 in for 1-3/8–1-3/4 in shafts). Woodruff keys and taper keys are u

Selecting a shaft key comes down to matching key type, material grade, and dimensional standard to torque, speed, and environment. Square, parallel, and Woodruff keys cover 90% of industrial duty; tapered keys suit high-shock applications. Shaft and keyway tolerances per ISO 773 / DIN 6885 govern fi
Sourcing industrial retaining rings in mid-2026 maps cleanly onto three supplier tiers: heritage European standards owners (Seeger-Orbis, DIN 471/472), Chinese DIN/GOST volume producers (Shanghai Eastern Waves, min order 1,000 pcs), and North American custom shops (Arcon Ring, Eaton-type profiles).
Retaining rings are sized by shaft or bore diameter, groove dimensions, and ring style — with internal, external, spiral, and wave variants each governed by DIN 984, MIL-DTL-27426, and GB 893.1 standards. Selection hinges on load direction, axial thrust, groove Machining, and duty cycle, not just di
For power generation duty, the correct retaining ring is a tapered, axial-hoop, heavy-section alloy steel ring matched to rotor bore and centrifugal load, with material grade, hardness, and NACE compliance dictating selection over catalog price.

Locking assemblies for power transmission are dominated by Chinese ODMs with keyless shaft-hub units starting at US$1–10/piece, while European locking-connector suppliers (LEMO, Hirose) hold the high-voltage/IP68 niche. Spec engineers can source from 1,000+ Made-in-China suppliers, MOQs of 1 piece,

Locking assemblies (shaft, plate, container) differ in torque capacity, bore range, and surface pressure. Sizing hinges on shaft diameter, applied torque, axial load, and fit tolerance. Selection follows a 4-criteria matrix: bore vs shaft, torque vs pressure, duty cycle, and mounting geometry.

For automotive powertrain and chassis assembly lines, a Z8-style keyless shaft locking assembly paired with Cr-V locking pliers and PTFE/silicone assembly lube delivers the most reliable torque transfer. Cr-V (chromium-vanadium) and CR-MO (chrome-molybdenum) clamping tools dominate the WORKPRO/Klein
Locking assemblies lock shafts, plates, and containers by friction or mechanical interlock; select by torque/axial load class, bore-vs-OD fit, duty cycle, and ISO 11691 / API 671 alignment needs.

Lock nut sizing hinges on matching thread standard (ISO metric coarse/fine, UNF/UNC, BSW), nominal diameter, grade, and locking mechanism to vibration, temperature, and corrosion duty. The 2026 industrial fastener market continues to favor nylon-insert and all-metal prevailing-torque types for gener

Belt tensioner sourcing in mid-2026 splits between European spring-loaded industrial units and Asian automotive timing/ribbed-belt assemblies. Specifying engineers should match tensioner type to belt geometry, load, and environment before comparing 9 cataloged brands and OEM cross-references.
Belt tensioner sizing hinges on belt type, span length, and arc of contact: use spring or hydraulic automatic tensioners on multi-rib serpentine drives, and dead-weight or screw take-ups on long-span flat belt conveyors. Match OD, width, and OE reference (e.g. MERCEDES-BENZ 6062000073 / FORD 4118964

Stainless AISI 304/316 automatic belt tensioners with IP66/IP69K housings, food-grade H1 lubricant, and EHEDG/3-A hygienic design dominate food and beverage conveyor retrofits through mid-2026. Specification paths split between spring-loaded, hydraulic, and sensorized pneumatic units depending on wa

For pharmaceutical lines, 316 stainless steel timing pulleys with HTD or GT2/GT3 curvilinear teeth and FDA-grade lubricants are the default spec. Avoid anodized aluminum in CIP zones and never use plastic (acetal/nylon) above 0.5 kW or in washdown.
Match the timing pulley tooth profile and pitch to the belt first, then size by torque, RPM and bore; standard profiles MXL/XL/L/H and S2M/S3M/P8M cover 2.5–25 mm pitch ranges, with material (aluminum vs steel) and bushing style driving final cost.
V-ribbed belt sourcing in mid-2026 is dominated by Chinese rubber-goods clusters in Ningbo and by Tier-1 IAM brands such as GATES, INA, RUVILLE, OPTIMAL and SNR, with EPDM and CR as the two competing elastomer systems.

V-ribbed belts are spec'd by rib count, effective length (mm) and PK/J profile; matching all three against OE part numbers is the single most reliable way to size a replacement for engine or accessory drives.

Multi-rib (PK/V-ribbed) belts deliver roughly 30% more power transmission and 25% smaller drive footprint than classical V-belts, with belt speeds up to 40 m/s, making them the default choice for compact, high-RPM water-treatment pump and blower drives. The right belt is matched by rib count (PK3-PK
V-ribbed belt selection hinges on three measured parameters — rib count, effective length, and matching tensioner geometry — plus OE cross-reference to the host engine. Match these against duty cycle, then verify against SAE J1459 geometry rules.

Flat belt sourcing in 2026 clusters heavily in Chinese industrial hubs — Shandong, Hebei, Guangdong and Zhejiang — with PU, PVC and rubber styles quoted from US$0.10 to US$99.00 per piece, and audited Diamond Members dominate the export channel on Made-in-China.com and Alibaba.

Flat belt sizing starts from power (kW), speed (m/s), pulley diameter and shaft centre distance; polyurethane flat belts with aramid/steel tension members reach 98% transmission efficiency and up to 30 t lifting load per Walther Flender data.
Flat belts for oil and gas service must meet strict oil resistance, tensile strength and ATEX/IECEx requirements; polyurethane, nitrile rubber and chloroprene are the three main constructions, with selection driven by ambient hydrocarbons, temperature, and pulley diameter.
Conveyor chain sizing starts with four hard numbers — pitch, ultimate tensile strength, working load envelope, and operating speed — then matches chain type (roller, welded pallet, trough/en-masse) to the conveyed product and environment. Stainless or galvanized steel covers most food, grain and was
Stainless-steel roller conveyor chains with 75–600 mm pitch and 29.4–529.6 kN tensile strength lead pulp-and-paper mill specifications, paired with lubrication-free, corrosion-resistant link assemblies for wet-end, dryer and reel-deck service.

Choose a conveyor chain by matching pitch, working load, environment and attachment layout to the application: roller chain for low-speed unit handling, drop-forged rivetless (X348/X458/X678, 76.2–102 mm pitch) for overhead trolley lines, welded steel (WR/WH series) and WD-series drag chain for heav
Silent chain (inverted-tooth) drives are sized by pitch, width, and horsepower rating, with selection driven by service factor, speed ratio, and operating speed. Standard pitch families range from 3/16 in to 2 in, with horsepower charts published by Ramsey and other OEMs.
Silent chain selection for aerospace power transmission hinges on ASME/ANSI B29.2M leaf-style standards, premium-grade alloy steels, and AS9100-controlled distribution channels such as Align Aerospace.

Silent chain (SC, 齿形链) is the right pick when a drive must run above roller-chain speed limits with low noise, low vibration, and synchronous timing. Selection hinges on pitch (commonly 9.525 mm and 12.7 mm), guide form, working load, and hub environment, with GB/T 10855 as the dominant Chinese refe
Silent chain drives pair inverted-tooth link plates with involute-form sprockets to cut noise vs roller chain, but the geometry is not yet covered by a single harmonised standard, so spec gates must be built from OEM catalogues, peer-reviewed geometry data, and material/process notes.

V-belts on sheaves and synchronous belts on toothed sprockets both transmit power between parallel shafts, but a V-belt is a friction device that can slip while a synchronous (timing) belt is a positive-drive mesh holding ~98% efficiency across the load range, per DOE guidance.

Industrial timing belts list from US$0.10–$2.00 per piece at 1,000-piece MOQ on Chinese B2B platforms (2026-07-15), while Gates POWERGRIP® trapezoidal chloroprene/HNBR belts deliver 150 kW at 10,000 rpm and ISO 19347:2015 compliance. Real cost is driven by tooth pitch, width, tensile cord, and tier.

Spec-driven timing belt selection hinges on tooth profile (T/HTD/STD/AT/RPP/TW), pitch, tensile-cord material, and operating environment; mismatches on any of these three shorten service life by 40–60% in documented automotive field returns.
Roller chain FOB prices on Chinese B2B platforms ranged from US$2.00–2.20 per meter for 08B-pitch transmission chain to US$10.00–20.00 per 100 m for ANSI C2052 hollow-pin conveyor chain as of 2026-07-14, with material, pitch and standard governing the spread.

Roller chain and timing belt are the two dominant positive-engagement power-transmission options; the right pick hinges on efficiency, environment, maintenance access and total cost of ownership, not on either being universally superior.

Roller chain selection in 2026 is governed by ISO 606/BS 228 pitch series, a 15,000-hour ISO rating life, and a 98% typical drive efficiency, with lubrication temperature windows from -40°C PAO greases to 650°C copper-graphite pastes shaping real-world service.
Roller chain selection starts with pitch, tensile rating and ISO 606 series: precision simplex ANSI/BS chains span 6 mm–76.2 mm pitch and reach 2 744 kN minimum tensile strength per D.I.D 2026 data.

Industrial shock absorber sizing is a kinetic-energy and impulse-rate problem solved by E = ½mv² ÷ η, validated through OEM software such as SMC's SAMSS selector and Enidine's Enisize tool, with hydraulic adjustable types dominating high-cycle automation.

Industrial hydraulic shock absorbers sized for data-center white-space loads (5-200 kg per server rack, 0.5-3 m/s impact velocity) are the default pick over automotive coilovers, with 100,000-1M cycle life ratings and M5-M20 thread bodies the gating spec line.

Hydrodynamic fluid couplings ship from a small number of specialised global makers, with a heavy concentration in China. Constant-fill and variable-speed units cover 500–1,800 rpm ranges for conveyors, fans, crushers and pumps.
For power-generation soft starts on conveyors, fans and pumps, a fixed-fill (traction) fluid coupling sized to roughly 105–110% of motor nameplate is the default; use a scoop-control (SCR 24/25/26) or scoop-trimming (GST/MST) unit only when load sharing or variable speed is required.

Fluid couplings are specified by matching motor starting torque (typically 150-200% of running torque) to driven load, with constant-fill units for soft-start and scoop-controlled variable-speed units for stepless output regulation over 500-1,800 rpm.
A correctly sized universal joint pairs torque, angle, RPM and bore diameter against an industry-standard series code; cross journals 23.8–41 mm cover most light-to-medium driveshaft applications.

Spicer 5-153X leads Amazon's automotive U-joint best-seller list at $20.45, with the 1310 and 1410 series dominating the top five by torque class. Selection hinges on series, yoke bore, and torque rating, not price.

Semiconductor fabs run tool drivetrains at 1-3° angular misalignment and sub-0.05 mm concentricity, which pushes engineers away from elastomeric and grid couplings toward gear and disc couplings that hold backlash and run clean.
Selecting a gear coupling starts with four numbers: service torque, peak torque, bore size, and operating rpm. Match those to AGMA-rated full-flex or double-engagement designs sized for your misalignment and environmental duty.
Jaw couplings are specified through 31 manufacturers and 85 products on DirectIndustry, with price points from US$2.49 per piece (MOQ 50) to US$20,000 per set depending on torque class and material. Sizing hinges on torque, bore, spider shore hardness and misalignment budget, not brand.
Bucket elevator selection is governed by material form (powder/granule/block), bulk density ≤1.6 t/m³, and four core structural variants — belt, chain, link-chain, and continuous — matched to ATEX zone, lift height, and ignition-risk monitoring.
Wire rope sling prices in 2026 span roughly US$1.00 to €244+ per piece ex-works, with galvanized 6×36-WSC grade 1770N/mm² slings at EN 13414-1 dominating the catalog; cost drivers are rope grade, leg count, end-fitting, length, and MOQ from China vs EU stock.

Wire rope sling selection hinges on matching diameter, construction (6x19 vs 6x36 vs 7x19) and end-fitting (eye-eye, eye-hook, Flemish eye) to the working load limit, with a 5:1 design factor standard for general-purpose lifts.
Roller conveyor selection is driven by four binding decisions — drive type (gravity vs motorized/chain), roller diameter, frame capacity, and conveyed load class — with current OEM catalogs spanning 225 manufacturers and 581 product lines (DirectIndustry, 2026-05-23).

Harmonic drive reducers deliver 30:1 to 320:1 single-stage ratios via flexible spline deflection, with zero backlash and 50% of volume of planetary units. Selection hinges on ratio, peak/continuous torque, hysteresis loss, input speed and lubrication regime.

Spherical roller bearings (SRB) are non-separable double-row radial units with barrel-shaped rollers that handle heavy radial load plus up to ~2° static misalignment. The metric 23000/22200/22300/24000/24100 series, built to DIN 616, DIN 635-2, ISO 492 and DIN 620-2, dominate heavy-industry picks.
Industrial spring selection hinges on matching load, deflection, material and environment: helical compression/extension/torsion dominate 80% of mechanical cases, while air springs and SAM shock absorbers cover vibration isolation. Specs to gate on are wire diameter, free length, spring rate (N/mm),
Shaft coupling selection in 2026 pivots on matching torque, speed, misalignment and environment to one of seven core families — rigid, elastomer/jaw, disc, gear, grid, bellows and chain — using published torque envelopes (e.g. 20–1,164 Nm disc, 46–358,000 Nm gear) and verified maker specs.

Industrial gear selection hinges on matching gear type, precision grade, material heat treatment, and load case to the application's torque, speed, and duty cycle, with custom large-diameter gears up to 96" and Grade 5 precision as the upper end of common commercial capability.

Electric linear actuators are selected on four gates: drive type (belt vs screw vs piezo vs voice-coil), force/speed envelope, guidance/bearing class, and feedback resolution. Match the gate to load, stroke, duty cycle and environment; verify moment loads and thermal expansion before committing.

Pneumatic conveyor systems range from ~₹14,000 entry-level MS-bodied Indian units to six-figure USD engineered lines; budget 5-15% for receivers/cyclones, 8-12% for blowers, and 20-35% for installation/controls.
Pneumatic conveyor selection hinges on phase (dilute vs dense), conveying mode (vacuum vs positive-pressure), material flow regime and distance: 2026 OEM line-ups from Delfin, Trelleborg and FIBRO span 1 kg to 2,400 kg load and 5–500 kg/h throughput, with 5.5–15 kW side-channel blowers driving long-

Screw conveyor selection hinges on matching trough geometry, screw pitch-to-diameter ratio, material-of-construction and drive torque to the bulk solid's density, abrasiveness and flow class. Shafted tubular/horizontal units dominate 1-30 m³/h duties, while shaftless spirals handle wet, sticky or fi

Chain conveyor selection hinges on matching drive topology, chain pitch, payload envelope and environment to the duty. Three recent OEM product entries (May 2026 MiniTec GKF modular, April 2026 CONVOYNORT 1200 Series overhead monorail, June 2026 MHE drag-chain) anchor the comparison.

Belt conveyor selection pivots on five engineered decisions: belt type, drive reducer class, idler/return system, safety guarding and material-handling duty. Specifying CEMA-grade bulk units (S7) or food-grade flat belts (S2) against wrong duty class causes 80% of early-life failures.
Selecting a cycloidal reducer hinges on matching torque class, output speed, shock-load rating, and shaft topology to the driven load. DirectIndustry lists 142 cycloidal models from 21 makers; torque spans 20 Nm to 5 kNm with output speeds 65-270 rpm.

Worm gear reducers cover single ratios 10:1-60:1 and double ratios 200:1-900:1 in cast-iron housings, with efficiency climbing toward 60-70% when bronze wheels run on hardened steel worms; selection hinges on duty cycle, mounting and washdown rating.
Helical gear reducers span 0.06 kW to 4,000 kW with torques from 500 Nm to over 10 kNm across coaxial, parallel-shaft and shaft-mounted topologies; selection is driven by shaft layout, torque class, ratio range, and IEC flange standard.

Planetary gearbox prices on public B2B platforms in Q2 2026 cluster from US$30–50 for 76 mm DC solar-tracker micro units to US$1,000+ for cast-iron Bonfiglioli-pattern units with splined shafts, with a P62m class FOB tier near US$80/piece at 10-box MOQ from Shanghai suppliers.
Planetary gearbox selection hinges on matching torque range, ratio, backlash and stages to the driven load. Coaxial, low-backlash units span 5-1,000 Nm at ratios to 350:1 across 1-3 stages.
A pillow block bearing pairs a housed insert bearing (UC-series) with a pedestal-style cast or pressed housing and is selected by bore size, load direction, shaft speed, sealing class, and housing material. UCP-series 40 mm-bore units weighing 1.9 kg with Gcr15 races typify the spec range currently
Linear bearing selection hinges on load profile, travel length, environment, and lubrication model; for ≤204°C clean or washdown duty, polymer-lined plain bearings with 316 stainless hardware are the default, while recirculating ball or crossed-roller guides win on rigidity and precision from 0.01 m
Tapered roller bearings split into single-row (TS/TDI/TDO), four-row, thin-section low-torque and case-hardened thrust variants; selection pivots on load direction, speed, and bore range like 1.26–2.07 in from RBC T-series.

2026 FOB price for spherical roller bearings spans roughly USD 0.0001–100 per piece across 22200/22211/22220/23120/239 series from Chinese exporters, with 222-series CC/W33 at USD 1–50, 22220C/W33 GCr15 at quoted FOB Shanghai, and 239-series at ~USD 19–26.

Deep groove ball bearing prices in 2026 span roughly US$1-50 FOB per piece for metric 6000-series, scaling with bore (3-400 mm), material (chrome steel vs ceramic), seal choice and ABEC tolerance. Procurement lead time runs 15-25 work days for export-pack orders.

Single-row deep groove ball bearings remain the highest-volume bearing type, with 139 of 140 catalogued radial ball bearing products on the 2026 DirectIndustry index listing the deep-groove geometry. For general-purpose radial loads at moderate speed, the 62-series (6200-6299) is the engineerin

Industrial spring unit prices on Made-in-China cluster between US$0.01–0.50 per piece for stainless extension/torsion springs at 1,000-piece MOQ, with garage-door torsion springs priced per kg at US$0.80–1.50, while India-origin compression spring makers quote wire 0.2–12 mm with negotiable MOQ.
Stainless 316L spider elements with FDA/EC 1935 nitrile or EPDM bodies are the spec baseline for jaw couplings on washdown mixer, pump and conveyor drives in food and beverage plants.
Jaw couplings (L-type /梅花/curved-tooth elastomer spiders) are the default low-cost general-purpose flexible coupling for pumps, fans, gearboxes and small servos up to roughly 70 kW and ~19,000 N·m peak bore size; pick them for torsionally soft, radial-misalignment-tolerant drives, not for high-torqu

Disc couplings handle 161,003 Nm peak torque and 9,000 rpm on large industrial flanged shafts, with ATEX-rated all-metal disc packs specified for process-pump and general industrial duty per current OEM catalogs.

Industrial clutch & brake assemblies range from US$8-15 per set for aftermarket friction plates up to US$168+ for OEM pedal assemblies, with hydraulically-actuated piston units priced on inquiry from Korean OEM Hawers Co., Ltd..

Friction clutches and electromagnetic brakes deliver precise torque transfer with discrete engagement, while fluid couplings transmit power through hydrodynamic drag — the 2026 spec choice hinges on start-up load, slip tolerance and overload behavior, not horsepower alone.
Specifying industrial clutch and brake packages in 2026 hinges on four levers: torque density, thermal capacity, duty cycle, and fail-safe engagement. This guide maps spring-set, electromagnetic, hydraulic, and pneumatic families against those levers, with price bands drawn from active 2026 listings
Universal joints handle angular misalignment up to 25-45° per joint; shaft couplings cover parallel/angular offset under 3° with higher torque density. Choose UJs for driveline articulation, couplings for inline motor-to-pump precision.

Flexible, disc, bellows and gear shaft couplings sit in distinct torque, misalignment and price bands; the 2026 sourcing map spans 94+ European OEMs on DirectIndustry and concentrated Hebei OEM/ODM hubs for commodity spider and gear types.

Shaft coupling selection is governed by five hard numbers — torque, speed, bore range, misalignment capacity and environment — with flexible elastomeric, gear, disc and jaw types covering roughly 70–90% of industrial drives.

Directindustry catalog lists 12 belt-drive, 15 ball-screw and a broad modular-class field of linear module makers, with Bosch Rexroth, Schaeffler/Ewellix, Güdel, NTN and KML leading the European tier and a dense China cluster led by FUYU, Grand Growth, Schenck-class suppliers and Yongrun covering 28

Pulp and paper mills specify linear modules with stainless rails, IP65 seals, food-grade grease and high-payload slides to survive steam, condensate, lint dust and caustic washdowns common to paper machines.

Crossed roller guides for aerospace must hit sub-arcsecond repeatability, vacuum-compatible lubrication, and -54 °C to +150 °C survival; the CSR series at 10.9–135 kN load and 15–45 mm size band is the most concrete spec set available for sizing the rest of the field against.

Ball spline selection is governed by shaft diameter, accuracy class, load rating, and stroke length; commercial spline shafts span 6–50 mm diameter with N/H/P grade options, while solid and hollow shaft constructions serve different rigidity and weight budgets.
Four industrial OEMs — Eichenberger, Helix Linear, Steinmeyer and Technische Antriebselemente — list nine bronze lead-screw variants on DirectIndustry, with diameter, lead and material class driving the 2026 supplier shortlist.
Lead screw sizing hinges on five inputs — axial load, lead, length, nut material and duty cycle — with efficiency bands of 30–70% for polymer nuts and 80–95% for ball screws. Match these to a defection and buckling check before picking drive torque.
Linear actuators and lead screws overlap but are not interchangeable: a lead screw is the drive element alone, while a linear actuator is the integrated assembly. Published 2026 specs show actuator force ranges reaching 35.8 kN (Tolomatic IMA) and lead-screw actuators hitting 5,000 N (MECVEL EC1), w

A 2026 linear actuator buyer's spec sheet must lock stroke length, dynamic load, duty cycle, IP rating and feedback type before chasing price; electric rod, ball-screw, lead-screw, belt, pneumatic and piezo classes serve non-overlapping load and precision bands.
Linear actuator selection is driven by four binding criteria — load force (N), stroke length (mm), duty cycle (%), and ingress protection (IP rating) — with 12V/24V DC units dominating below 2000 N and 220V AC or pneumatic units covering 2000–15000 N industrial service per OEM catalogues.

China's Shandong cluster dominates volume ball-screw supply, with C7 ground screws listed at US$7-12/piece and support units at US$5-291; HFQ (Hiwin-compatible) 20mm linear guides and 3205-series rolled/ground screws lead OEM sourcing. Selection hinges on ISO/DIN 69051 accuracy grade, lead, and end-

For chemical-processing duty, specify ground ball screws in 440C or 17-4 PH stainless with PTFE or graphite-filled nuts, EPDM/FKM wiper seals, and at least 304 stainless wipers; flanged, zero-backlash designs rated above 0.5 m/s suit valve actuation, metering pumps and CIP linear slides.

Ball screw selection hinges on matching load, accuracy class (C0–C10), lead, DN value, and duty cycle to the application; a ground C5/C7 screw typically suits general CNC, while a C3 or C0 rolled-ground is required for machine-tool axes.
As of July 2026, 6 belt-driven linear guide makers and 7 dovetail linear guide makers are listed on DirectIndustry, while Made-in-China and Alibaba show 100+ active suppliers for square and high-precision linear guide rails, dominated by Chinese factories.

Slewing drive sizing is governed by five mechanical loads: axial, radial, tilting moment, holding torque, and output speed. Standard OD bands run 300–5000 mm across single-row ball, crossed-roller, double-row ball, three-row roller, and thin-section constructions.

For power-generation slewing drives, specify worm-gear dual-axis units sized to holding torque and tilting moment, IP66 sealing, and gear ratio matched to tracker slew rate, not to panel size.
Slewing drives are worm-gear or epicyclic gearboxes rated by output torque from ~1 kNm solar trackers up to 350+ kNm offshore cranes, and selection pivots on torque, moment load, IP, self-locking, and backlash class.
10 manufacturers across DirectIndustry list motor variable-speed drives in three-phase, vector and digital form factors as of 2026-06-09, while Made-in-China lists VFD entry prices around US$100-202 per piece on June 2026 listings.
Variable Speed Drive sizing starts with the motor's kW, service factor, and load curve; matching V/Hz, torque profile, and enclosure to the driven machine trims energy cost 20–50% versus throttling.

Variable speed drives for automotive lines run from 0.4 kW lab units to 6 MW test-cell rigs, with V/F, sensorless vector and full flux-vector control tiers. Voith, V&T EcoDriveCN and ABB ACS/Siemens SINAMICS families dominate the 2026 shortlist.

Variable speed drives (VSDs) match motor speed to load via electronic or hydraulic control, and a 2026 spec-driven selection hinges on load profile, enclosure/IP rating, harmonics, and bus protocol rather than brand alone.
Helical gear reducer sourcing in 2026 is dominated by Chinese OEM and trading hubs on Made-in-China and Alibaba, with Zhejiang and Jiangsu clusters leading parallel-shaft, helical-bevel and helical-worm output for global distributors.

Helical gear reducers in 2026 ship with 11–190 kW power bands, 5–10 kNm torque, hardened-and-ground alloy gears, and modular housings sized by AGMA/ISO 6336 service factors. Selection hinges on service factor, ratio, mounting style, and duty cycle, not price.
Stainless 304/316 RV reducers with IP66 sealing and food-grade lubricant run conveyors, mixers and palletisers in F&B plants; avoid cast-iron housings and white-mineral-oil grease in washdown zones.

Harmonic drive reducer sourcing in mid-2026 clusters around Chinese ODMs in Shenzhen, Wuxi, Guangzhou and Hangzhou, with FOB unit pricing on Made-in-China spanning roughly US$100–400 per piece for zero-backlash robot-joint models. Harmonic, RV cycloidal, and planetary reducers run on distinct kinema

Harmonic-drive reducers deliver single-stage ratios of 50:1 to 100:1+ with near-zero backlash; size them on rated torque (N·m), ratio, transmission error (arcsec), input speed (RPM) and service-life duty cycle.

A harmonic drive reducer is a strain-wave gear whose elliptical wave generator, flexspline and circular spline deliver zero-backlash reduction ratios typically between 30:1 and 160:1; pick one by torque, ratio, backlash grade, life, input type and lubrication envelope.
Cycloidal reducer sourcing on Made-in-China and Alibaba lists 382+ China factories, MOQ 1 piece, FOB price band US$29-1,479; major clusters in Jiangsu, Zhejiang, Guangdong, audited ISO 9001:2015 suppliers dominate export flow.
Selecting a cycloidal reducer hinges on matching ratio range, torque capacity, and shock-load behavior to the driven load, with 21 industrial manufacturers currently listing 142 models across directindustry listings.
Industrial gear landed prices in mid-2026 span roughly US$0.50 to US$12.80 per piece on Made-in-China for low-tier agricultural castings, with spur/spur replacements for handheld power tools listing near INR 487 (about US$5.80) on Indian B2B sites. Material, tolerance class and supplier tier drive t
Industrial gear buying in 2026 is driven by application class, AGMA/ISO/DIN standard match, and duty-cycle rating; the right pick balances torque density, backlash, lubrication and supplier QA, not price alone.
Industrial gear selection hinges on four spec gates — service factor, pitch and module class, mounting form factor, and lubrication regime. Spur, helical, herringbone, bevel and worm sets each map to a distinct duty envelope defined in ISO 6336 and AGMA 2001.

Worm gear reducers span €43 for a 60 mm cast-iron WPDS unit to multi-thousand-euro modular right-angle drives rated 1-2 kNm. Sourcing volume, torque class, ratio range, and module vs S-series build drive most of the price spread.

Worm gear reducers and harmonic drive (strain-wave) reducers sit at opposite ends of the precision-torque spectrum: worm units deliver single-stage ratios up to ~4,900:1 with torques exceeding 10 kNm for roller mills and conveyors, while harmonic units cover 20 Nm to over 10 kNm with zero-backlash c

Worm gear reducers transmit motion at right angles with single-stage ratios from 2.5:1 to 100:1, torques from under 5 Nm to above 10 kNm, and powers from 0.06 kW to 335 kW; the 2026 buy hinges on ratio, torque class, housing material and duty cycle.

Worm-gear reducer selection is governed by four hard numbers: output torque band, ratio, mounting geometry, and duty cycle, paired with housing material and lubrication choice. Right-angle worm units cover 1–10 kNm and ratios from 5:1 to 100:1, with die-cast aluminum for light loads and cast iron fo
Planetary reducer supply in mid-2026 is dominated by Chinese OEM clusters in Jiangsu, Guangdong and Shandong offering 50:1-160:1 ratios, with micro units priced US$ 285-300/piece FOB and integrated linear-planetary drives at US$ 190-243/piece MOQ 1.

Planetary reducers in 2026 ship across 1:3 to 1:4000 ratios with output torque bands from 260 kN·m class to 2,600 kN·m industrial units. Selection pivots on torque, ratio, backlash, radial load, and service factor, not on a single vendor.

For aerospace duty, planetary reducers are typically qualified on torque density, backlash below 5 arc-min, single-stage efficiency above 97%, and a documented low-outgassing lubricant path; Neugart PLPE, PMP PMB, and harmonic CSG units cover the bulk of current servo and actuator asks.
Planetary reducers are specified by torque density, backlash (often 8 arcmin or less for precision stages), ratio range (commonly 3:1 to 100:1 single-stage, up to 10000:1 with helical pre-stages), service factor, and radial/axial load — selection is driven by duty cycle, accuracy class, and mounting
Gearbox sourcing in 2026 is dominated by China clusters: Made-in-China lists 2,000+ industrial gearbox manufacturers offering reducers from US$50/piece, Taizhou focuses on NMRV worm and RV helical units in ADC12/HT200 housings, Jiangyin Deling supplies plastic extruder and rubber gearboxes, and spec
Luoyang, Henan hosts the densest slewing bearing OEM cluster, with single-row four-point contact ball, double-row ball and three-row roller units priced US$365-500 FOB per piece on Made-in-China (June 2026). Cross-roller and custom configurations ship in small batches from ISO 9001:2015 aud
A slewing ring bearing is selected by bore, OD, static load rating, dynamic load rating, gear type and rolling-element family, with diameters spanning 200 mm to 5000 mm and standard duty classes covering 4-point contact ball, crossed roller, three-row roller and internal/external gear variants.
Mining-duty slewing ring bearings are typically single-row four-point contact ball or crossed roller designs in 42CrMo or 50Mn forged rings, with integrated external or internal gear teeth, diameters from ~500 mm to 5 m, supplied mainly by Chinese OEM/ODM clusters in Luoyang, Xuzhou and Hefei at FOB

Hybrid ceramic (steel races + Si3N4/ZrO2 balls) and full-ceramic (Si3N4, ZrO2, Al2O3) bearings are sourced in volume from Chinese OEM/ODM clusters in Shanghai, Zhejiang and Fujian, with FOB price bands of US$0.29–US$25 on 6000–6300 series deep-groove and 6900/697 miniature sizes as of July 2026.
DirectIndustry lists 20 spherical plain bearing manufacturers across 56 catalog SKUs, while Made-in-China clusters show Zhejiang and Fujian OEMs offering GE-series radial rod ends from US$0.30–45.00 per piece at 100–1,000-piece MOQs as of 2026-07-05.

Spherical plain bearings are sized by load case (radial, angular, axial), bore diameter series per DIN ISO 12240-3, and sliding-contact material (steel/PTFE, steel/PTFE-fabric, steel/steel). Bore ranges 10–360 mm cover most industrial specs.
Spherical plain bearings are sliding-contact, self-aligning assemblies selected by load direction (radial, thrust, or angular), material pair (steel/steel, steel/PTFE, steel/brass, stainless/PTFE), and lubrication regime. Steel-on-steel (MB, SB-OK) handles heavy oscillating radial loads; PTFE-lined

China-origin pillow block bearing supply is concentrated in Shandong and Hebei, with UCP/UCPF/UCPFL series insert units in bearing steel and chrome steel GCr15 dominating 2026 OEM output, and MOQ bands starting at 1–5 pieces for standard catalog items.

For power-generation duty, specify 2-bolt or 4-bolt pillow block bearings with set-screw or adapter-sleeve insert locking, chrome-steel AISI 52100 (Gcr15) rings rated above 4000 rpm, relubricatable housings and IP55 sealing; UCFL/UCP/UCPH series from Chinese OEM hubs such as Xiamen Zogbearing, Hebei

Pillow block bearings are mounted bearing units in cast iron, pressed steel, stainless or polymer housings; selection hinges on shaft bore, load case, mounting style and sealing class. Shaft size and series codes (UCP, UCFC, UCT, HCP, SBPP) drive interchangeability, not the housing brand.

Shandong and Jiangsu remain the dominant Chinese tapered roller bearing manufacturing clusters, with Liaocheng alone hosting multiple ISO 9000 suppliers offering 25877/25820, 33112 and 3820/950 four-row series. Buyer specification hinges on row count, precision class P0–P6, and OEM/ODM customisation

Tapered roller bearing sizing pivots on combined radial-plus-thrust load case, ABEC/P0-P6 tolerance band, and a single-row steel envelope; inch and metric series share the same cone-cup logic, and 2026 supply is tightening as the NTN-NSK integration MoU reshapes Asian capacity.

For automotive tapered roller bearings, single-row GCr15 chrome-steel units in 30–72 mm bore with ABEC-3 to ABEC-5 tolerance remain the workhorse for gearbox and wheel-hub service, priced US$0.10–3.50 per piece FOB China on 2026-06 listings.

Tapered roller bearings combine radial and axial load capacity in one separable assembly, with single-row units handling primarily radial load and double-row or paired sets taking combined thrust. Selection hinges on bore/OD/width envelope, dynamic load rating, ISO 15/ABMA tolerance class, and steel
Self-aligning bearing sourcing is dominated by 25+ active manufacturers and 456+ China-based roller suppliers; selection hinges on bore, misalignment angle, material and housing. Shandong and Shanghai clusters lead exports.

Self-aligning bearing sizing hinges on bore (10-160 mm), load direction (radial with minor axial), misalignment tolerance (typically 1.5-3°), and housing material (cast iron, pressed steel, stainless); food-grade and stainless variants extend temperature and corrosion envelope per SAE AS81936 and EN

For semiconductor tool builders, self-aligning ball bearings in 440C or Si3N4 ceramic with ABEC-5+ tolerance and cleanroom-class lubrication dominate wafer-handling and CMP applications, while polymer igubal units only suit low-load, non-vacuum zones.

Self-aligning bearings tolerate 1.5°-3° static shaft misalignment through a two-row ball geometry with a spherised outer race; selection is driven by load direction, misalignment budget, housing type and food/corrosion exposure rather than bore size alone.

Shandong's Linqing/Yandian cluster and Jiangsu's Wuxi remain the two anchor supply bases for angular contact bearings in July 2026, with audited Made-in-China entries spanning 7002 through 5312 series at MOQs from 1 to 10 pieces and FOB bands from US$1.00 to US$10.00 per piece.
Angular contact bearings are specified for combined radial+axial loads, paired in opposing sets, with contact angle (15/25/40°) as the dominant sizing lever. Single-row units must be matched, while two-row axial types (ZKLFA series) integrate screw support. Selection pivots on contact angle, preload
Angular contact bearings carry combined radial+axial loads; choose by contact angle (15°/25°/30°/40°), preload class, ABEC/ISO tolerance, and matched-pair arrangement. Single-row steel units span 17–120 mm OD and reach 800 mm OD in custom planetary-gear builds. Two-row units dominate balls
Linear bearing unit prices in 2026 span roughly USD 17–22 per piece for Chinese OEM 12 mm closed stainless self-aligning bearings, while NTN miniature 7 mm corrosion-resistant ball-guide units and Thomson Linear Ball Bushing lines sit in mid-to-high OEM tier; total cost-of-ownership is driven by sha
Linear bearings and tapered roller bearings solve different motion problems: linear bearings carry sliding/rolling loads along a shaft (typical OD ranges 1.38–10.53 in), while tapered roller bearings handle combined radial+axial loads on rotating shafts. Match by motion type, load vector, stiffness
Linear bearing selection in mid-2026 is driven by three decisions: bearing type (ball bushing vs crossed-roller vs profiled rail), shaft/rail class (hardened ground 52100, stainless, aluminium), and load envelope. PBC Linear SB24, STAF MBX, norelem 21505 and Thomson Ball Bushing families define the
Thrust bearings transmit axial load along the shaft; the 2026 buying decision hinges on load type (ball vs roller), speed envelope, alignment tolerance and lubrication regime. Roller thrust handles 3-5x the load of equivalent-size ball thrust, but caps at roughly 25% of the ball unit's permissible s
Thrust bearings are rolling elements built to carry axial loads along the shaft axis, with subtypes (ball, roller, needle) selected by load magnitude, speed, alignment tolerance and lubrication regime per OEM catalogs dated May-July 2026.
Roller bearing sourcing in mid-2026 is dominated by 2,000+ China-based manufacturers offering bearing-steel cylindrical, tapered, needle and crossed-roller types priced US$1,500–5,000/set MOQ, with ABEC-1/3/5 precision and C0–C5 clearance as the standard buyer-side selection vocabulary.
Roller bearing sizing starts with three numbers — dynamic load rating C, equivalent dynamic load P, and target L10 life — then narrows by type, clearance, lubrication and seal. A 45 mm four-row recirculating roller guide rated 11,300–572,700 N illustrates the load envelope engineers work within.
China-origin ball bearing sourcing on Made-in-China, Alibaba and WTOO lists deep-groove, angular-contact, thrust and unitised variants from 6003-class miniature up to 6407-series heavy-industrial sizes, with thrust lines like 81211 at US$0.85–1.30/piece MOQ 1,000.
Shaft keys and taper bushes are the two dominant shaft-to-hub fastening methods in 2026, with parallel keys dominating low-torque drives and taper bushes dominating V-belt and sprocket assemblies above 5 kW.
Ball bearing selection pivots on six hard gates — load rating, speed limit, misalignment tolerance, lubrication, fits/clearance, and environment — with deep-groove, self-aligning, angular-contact, ceramic-hybrid and ceramic types mapped to those gates.
Rolled ball screws typically run US$30–68 per piece at MOQ of 5 in China (2026-05), while precision-ground units reach 5–10x that; total cost is driven by lead accuracy class, preload, and end-machining.
Ball bearing selection on a 2026 shop drawing hinges on six spec gates: load type and magnitude, speed limit, fit and tolerance class, lubrication, sealing, and operating temperature. Get any one wrong and the bearing fails; get them all right and a 608 or 6203 sized part under USD 6 will outlast an
Disc coupling landed cost in 2026 spans roughly US$9.80 to US$198 per set at Chinese wholesale MOQ, while Lovejoy MD-series stainless and aluminium units list on DirectIndustry with material, torque and configuration gates that drive price 2-3x between the same bore size.
Spring-loaded belt tensioners and roller chains solve two different jobs: tensioners maintain belt wrap force on ribbed or V-belt drives, while roller chains transmit positive power between parallel shafts via sprocket pitch. Selecting the wrong one destroys either the belt or the sprocket in days.
Select pillow block bearings on housing material, dimensional series and insert type first; 2026 sourcing windows on Made-in-China.com show UCP/UCFL/UCS plastic-housed inserts at US$2.20-5.60 and steel housed units at US$0.50-100.00 with MOQs from 1 to 1,000 pieces.
Locking assemblies in 2026 split into three distinct procurement tracks: mechanical shaft-locking elements (DIN-style, keyless bushing family), electrical push-lock cable connectors, and retractable-pin load-rack interlocks. Spec the wrong family and the assembly fails in service.
V-ribbed belt selection rests on seven load-side criteria: rib count 3–9, effective length, top width, EPDM vs CR compound, tensioner and idler stack, ISO 4184 / DIN 7867 geometry, and ambient envelope.
Tapered roller bearings transmit combined radial + axial load through angled rollers; the 2026 buy hinges on series (TS/TDO/TDI), bore 0.5–10.5 in, tolerance class P5/P6, and matched cone-cup pairing per ISO 492.
Ball bearing selection in 2026 hinges on six hard gates: load type and direction, RPM, ABEC tolerance class, cage and seal choice, material (chrome steel vs stainless vs ceramic), and lubrication regime. Get the gate order wrong and the bearing fails before L10 life is reached.
Gear couplings transmit torque permanently between two shafts; clutches and brakes control torque on demand. Use gear coupling for continuous drive service, and clutch-brake units for cyclic start/stop, hold, and indexing motion on a single shaft.
Helical gear reducer selection turns on five engineering gates — service factor, ratio/mounting, shaft arrangement, lubrication, and material grade — with 1–3 stage units from Siti covering >10 kNm coaxial torque under heavy load.
Self-aligning bearing selection pivots on misalignment tolerance, load direction, and housing material: choose double-row ball units for shaft deflection under 1.5–3°, spherical roller units for heavy radial load, and stainless or PTFE-lined units for food/aerospace duty.
Jaw coupling selection hinges on four engineer-controlled variables: torque rating, bore fit, misalignment budget, and elastomer spider durometer. Match service factor to driver/load class, then verify hub material, balance grade, and ATEX/IECEx zone rating for the actual install.
Planetary reducers dominate sub-10 Nm precision robotics with 0.1-arc-minute backlash options, while cycloidal units cover 200 Nm to over 10 kNm with shock-load tolerance; selection hinges on torque density, backlash, and duty cycle.
Linear guides and ball screws serve distinct roles in precision motion: linear guides handle load carriage with stroke up to 1200 mm, while ball screws convert rotary to linear motion with repeatability around ±0.006 mm per recent actuator specs.
Crossed roller guides carry load through 90-degree crossed cylindrical rollers between two V-ground races, giving 4-way equal load capacity in a single compact block. Select on roller size, accuracy grade, preload class, and runout.
Shaft collar pricing in 2026 is driven by three levers: material grade (steel vs stainless vs acetal/Delrin), bore size and tolerance, and mounting style (set-screw vs one-piece clamp vs two-piece clamp). Catalog prices span roughly USD 3-50 per piece for carbon-steel one-piece clamp collars and USD
Conveyor chain selection resolves to four spec gates — chain type (roller, slat, drag/cable), pitch and breaking load, environmental hardening, and supplier quality system — with ISO 9001 certified mills, hardened pin bushings, and stated material grades as baseline acceptance evidence.
Planetary reducers are selected on torque density, backlash class, ratio range and input-speed ceiling, with coaxial planetary units (e.g. RPL050) covering 5–10 Nm at the low end and harmonic-RV stages extending ratios beyond 100:1.
Flat belts and V-ribbed belts (PK/EL profiles) target different drive envelopes: flat belts suit low-pulley-diameter, high-speed, low-horsepower lines; V-ribbed belts combine flat-belt flexibility with V-belt wedging for compact, high-torque serpentine drives up to 8-rib configurations.
Cycloidal reducers in 2026 split into two sourcing channels: engineered precision units (Sumitomo Cyclo Drive, Spinea, Nabtesco-class) for zero-backlash robotics, and high-volume Chinese OEM units (Guomao Lide, XINLAN, Aokman) at US$76–1,479 FOB. Selection pivots on ratio range 30:1–119:1, torque en
Industrial locking assemblies for shaft-hub power transmission list at roughly $40-$400 for carbon-steel shrink-disc or taper-bush units in 2026, with stainless variants reaching $700-$2,000 and heavy-duty mining-class units above $5,000. Total cost-of-ownership is driven by material grade, bore siz
For 2026 sourcing, a harmonic drive reducer is selected on ratio (30-160), rated torque (8-1200 N·m), backlash class (≤3 arcmin standard) and wave-generator type. Chinese OEM CSF/CSG-class units compete on cost, Japanese Harmonic Drive Systems sets the precision benchmark for robotics and machine to
Jaw coupling prices in 2026 split into two clear bands: low-end Chinese OEM elements (L075/L100/L150 spider) list at US$2.49–6.59 per piece at 50-piece MOQ, while complete Lovejoy-class jaw couplings in sizes L035–L150 sit at US$3.99–90.00 on B2C surplus channels. Drive type, bore
Industrial shock absorber selection pivots on five engineered parameters: stroke length, energy per cycle (Nm/cycle), effective mass, damping profile, and mounting geometry. For 2026 sourcing, hydraulic vs pneumatic vs elastomeric vs magnetic-EDC types align to different cycle rates and environments
V-ribbed belt selection in 2026 hinges on rib count, deflection-pulley diameter and OEM cross-reference, not brand alone; current catalogue data shows 6-rib EPK profiles dominate at 70-90 mm pulley OD across European and Asian passenger-car fitments.
Variable speed drive (VSD) prices in 2026 span roughly USD 200 for sub-1 kW V/FD units to over USD 50,000 for 1 MW+ low-voltage drives, with mid-range 5–30 kW units typically USD 1,200–4,500 before installation and option costs.
Rotary ball bearings and linear ball bearings share the same rolling-element principle but solve orthogonal motion problems. Selection hinges on load direction, stroke, misalignment tolerance, and stiffness, not interchangeable interchangeability.
Ceramic bearings in 2026 sit across three very different buyers: low-cost Si3N4 hybrid skateboard/bike units at US$0.50-2.00 from Chinese trading hubs, and high-purity SSIC/ZrO2 precision parts (pump/valve/magnetic-pump components) from specialised manufacturers such as Beijing Zhongxing Shiqia
Disc couplings are specified for zero-backlash, high-torsional-stiffness drives; 2026 sourcing spans flange-mount 100–440,000 Nm (Lovejoy SX) to compact flange units 72–4,298 Nm (RENOLD Discflex) at US$9.80–198 FOB China.
Industrial gearboxes and industrial gears are distinct procurement categories: a gearbox is a sealed speed/torque conversion assembly, while an industrial gear is the bare precision-machined tooth component used inside or alongside it. Selection pivots on input speed (typically 750–3000 rpm), servic
Slewing bearings handle combined axial, radial, and moment loads in diameters from ~0.4 m to 12 m (integral) and up to 20 m (split), while thrust bearings are flat axial-only units typically under 1 m. Choose slewing for slow-rotation, multi-load platforms; choose thrust for pure axial load on rotat
Chinese cycloidal reducer factories list 382 manufacturers with 1,146 SKUs as of 2025-12-15, while June 2026 industrial catalogs show X/BWD pin-gear units starting around USD 80 FOB and precision cycloidal drives climbing past USD 4,000 at low ratios.
Industrial gearbox selection hinges on matching service factor, gear type, ratio, mounting and lubrication to the driven load, with 6-7 spec gates decided before vendor contact in 2026 practice.
2026 factory-gate prices for slewing ring bearings span from $100 to over $2,000 per set, driven by rolling-element type, gear form, bore-diameter, and whether the unit is single-row ball, four-point contact, crossed roller or three-row roller.
Spherical plain bearing selection hinges on four engineering gates: load direction (radial vs angular), material pair (steel/steel, steel/bronze, steel/PTFE fabric), lubrication regime, and compliance with ISO 6126 dimension series. Match these to swing, tilt, or oscillation duty.
Roller bearings carry higher radial loads via line contact, angular contact bearings handle combined radial+axial loads through controlled contact angle. Selection hinges on load direction, speed, rigidity and misalignment tolerance.

Ball splines and crossed roller guides both transmit moment and force along a single shaft, but a ball spline is a rotary+linear element rated for torque transmission while a crossed roller guide is a pure linear slide. Selection hinges on whether the application needs shaft rotation, moment stiffne
Lead screws and ball splines solve different jobs on the same axis: lead screws convert rotation to thrust at 30-95% efficiency with no recirculating hardware, while ball splines transmit torque plus axial/radial loads via a grooved shaft and ball-retained path.
V-ribbed belts drive accessories via longitudinal ribs that contact a smooth-faced pulley; timing pulleys use toothed grooves that mesh with a toothed belt for zero-slip, fixed-ratio transmission. Pick V-ribbed for compact, high-speed, low-noise accessory drives; pick timing for synchronised shafts
Harmonic drive reducers use three flexing components — wave generator, flexspline, circular spline — to deliver zero-backlash ratios from 30:1 to 320:1:1 in a frame one-third the size of equivalent planetary units.
Auto belt tensioners for 2026 spec at 60-80 mm pulley diameter, 29-40 mm arm height, and 30000-50000 km warranty, with chrome-steel/Gcr-15 bearings at P6 tolerance under TS16949 or ISO9001.
Variable speed drives (VSDs) and planetary reducers solve different problems on a motor shaft: a VSD throttles electrical frequency to vary output RPM, while a planetary reducer trades RPM for torque through a fixed gear ratio. For 2026 line builds, pairing an electronic VSD with a planetary stage i
FOB China industrial roller bearings sit in a wide USD 0.30–150.00 retail band per piece on Made-in-China.com listings, with tapered 33019/Q / 33209/Q at the 95×145×39 mm size class, and spherical 22220C/W33 in 100,000-piece monthly capacity from Shanghai.
Taper bush and lock nut both fix power-transmission hubs to shafts but solve different problems. Bush sizes 1008-5050 clamp with 1.5°-8° taper via axial bolts; lock nuts thread onto shafts and add 0.05-0.20 mm axial preload.
A helical gear reducer is a single-function speed/torque conversion unit defined by helical-tooth geometry, while a gearbox is the broader system housing that may carry helical, bevel, worm or planetary stages. Specifiers should match by torque band, shaft orientation, efficiency and stage count rat
Harmonic Drive reducers span roughly US$100-400 per piece at small frame sizes, climbing past US$3,000 for Harmonic Drive Systems CSF/CSG units and above US$10,000 for complete CSF-2UH or FHA servo actuator assemblies as of mid-2026 sourcing data.
Helical gear reducers in 2026 span 0.36-287 kW input and 500 Nm to over 10 kNm torque across parallel-shaft, hollow-shaft, shaft-mounted and solid-shaft configurations; selection hinges on torque class, ratio range, mounting and ATEX need, with FOB China pricing from roughly US$10 to US$447 per unit
Angular contact bearing selection is governed by contact angle (15°/25°/40°), load direction, speed rating, and mounting arrangement (single, DB/DF/DT matched pairs, or universal flush-ground). China-sourced 7000-series units listed in 2026 trade catalogs span US$0.78–135.70 per piece with MOQ from
Drum-shaped gear couplings list at roughly 1.00 万元 (≈USD 1,000+) on Chinese manufacturer sites as of May 2026, while forged gear-shaft coupling forgings on Made-in-China span US$ 0.10–1.00/piece MOQ 1 to US$ 767.86–921.42/piece MOQ 10, with size, material, heat treatment and brand dictating the spre
Helical gear reducer factory-direct export prices cluster around US$200-2,000 per unit on 2026 Made-in-China listings, with size, ratio range and shaft orientation the dominant cost levers.
Harmonic Drive reducers and variable speed drives solve different problems: harmonic gearing is a high-ratio mechanical reducer (~30:1 to 320:1) using elliptical flexspline deformation, while a VSD is an electronic motor-speed controller. They are complementary, not substitutes.
Industrial fluid couplings for pumps, motors, fans and conveyors typically range from low-hundreds to low-thousands USD per unit, with the four biggest cost levers being rated power (kW), impeller/blade design (constant-fill vs variable-fill), OEM brand premium, and certification scope (ATEX/IECEx).
Angular contact bearings handle combined radial+axial loads at higher speeds; pillow block bearings are housed units for shaft support on frames. Pick angular contact for precision spindles, pillow blocks for general conveyor/shaft mounting.
Silent chain (inverted-tooth) and conveyor chain solve different problems: silent chain for high-speed timing and power transmission up to ~10 m/s, conveyor chain for slow heavy-load material handling from DIN 8165 FV to SMS 1698 welded-mill types. Selection hinges on speed, pitch, environment and s
Crossed roller guide unit prices span roughly $6.99 to $665.96 per set in 2026 retail listings, with the widest cost lever being rail length (50-1500 mm) and load rating (90 N to 135 kN), per OEM and distributor data.
Square and parallel-machine keys run $0.20-$15 per piece FOB China in July 2026, with custom alloy variants reaching $50-$120 and stocked 4140/1045 steel blanks dominating 80% of the buy volume.
2026 VSD buying hinges on a fixed converter topology match: V/F for pumps/fans, SVC or VC for conveyors/mixers, DTC for high-dynamic hoists. Three gates decide model: rated shaft kW, supply (1/3-phase, 200-480 V), and control protocol (Modbus, Profinet, Ethernet/IP).
V-ribbed belt retail spans €6.64–€7.90 per piece for small industrial planer fitments (Dictum, 2026-06-18), GBP 12.07 for a Bosch 1 987 947 821 automotive alternator belt (eBay, 2025-12-12), and sub-USD factory pricing from Zhejiang mills running 4 million belts/year capacity (made-in-china, 2010-07
Selecting a gear coupling hinges on matching continuous torque, peak/shock factor, bore fit, alignment tolerance and API/AGMA service class to the driven train, not on catalog maximum torque alone.
Industrial lock nut pricing 2026 hinges on four spec levers — diameter/thread, material grade, lock type (DIN 980/982 nylon-insert, DIN 985, all-metal), and order quantity. China-made bearing lock nuts start at US$1.00/set MOQ, with volume breaks driving per-piece cost down at 100,000-set month
Crossed roller guides and linear modules are not interchangeable: crossed-roller rails deliver high rigidity in a compact envelope with limited stroke, while linear modules integrate a drive, bearing, and frame for longer travels. Choose the rail for short-stroke precision; choose the module for sel
Acme, ball and roller lead screws differ in load, speed, efficiency and cost; selecting the right type for a 2026 build requires matching duty cycle, precision, environment and standard compliance before vendor shortlisting.
A disc coupling is a torque-transmitting shaft connector that accommodates misalignment through stacked metallic discs; a shock absorber is a damping device that dissipates kinetic energy via fluid or friction. They solve different problems and are not substitutes in driveline design.
Wholesale tapered roller bearing prices on Made-in-China span US$1.00–10.00 per piece for hub-wheel types and US$1,500–5,000 per set for industrial rolling-mill units as of May 2026, with size, row count and material grade as the dominant cost levers.
Slewing drives in 2026 span roughly US $150 for light-duty worm units to over US $5,000 for solar-tracker gearboxes, with mid-range 7-25 inch enclosed-housing models clustering near US $500-1,500 FOB China; cost drivers are gear geometry, sealing, mounting interface and tracking-system compliance.
Slewing bearing selection collapses to four load-case gates — axial, radial, moment, and tilting — gated by raceway type (4-point contact ball, cross-roller, 3-row roller), gear form, and sealing, with bore sizes spanning 100 mm to 5000+ mm across surveyed 2026 OEM catalogues.
Spherical plain bearing prices in 2026 span roughly US$0.10 per piece for Chinese-made GE/GZ commodity sizes to US$5+ for DIN ISO 12240 series K steel/PTFE or angular-contact units from European brands; total outlay is driven by material pair, bore size, tolerance class, and MOQ tier.
Industrial shock absorber procurement in 2026: hydraulic small-bore (M8-M14) units dominate at US$2-5 FOB per piece, automotive OE rear-axle dampers (KYB 349134 type) sit in a separate spec class, and energy-per-stroke (Nm/cycle) plus cycle life are the two non-negotiable decision gates.
Spherical plain bearings handle misalignment on small shafts with bore IDs from 5 mm to 50 mm (DIN ISO 12240-1); slewing bearings carry axial, radial and moment loads on turntable-scale equipment where diameters run from tens of cm up to several metres. The two families meet at different scale
Silent chain (齿形链/inverted-tooth chain) list pricing in 2026 spans roughly 8-160 USD per meter for standard carbon-steel simplex 08B-24B pitch, with duplex and corrosion-resistant variants scaling 1.4x-3x higher by spec.
Roller bearing selection pivots on six hard gates: load type (radial vs combined vs thrust), speed rating, misalignment tolerance, lubrication regime, fit class, and housing rigidity — wrong on any one gate kills the bearing in service.
Steel lead screws span roughly US$20–300 per piece FOB Shanghai at low MOQs (1 piece), while complete lead-screw lift assemblies price at US$5,500–9,200 per set with 1-year warranty, per Made-in-China listings dated 2024-10-31 and 2019-07-26.
Cycloidal reducers deliver 30-60% higher single-stage reduction ratios and superior shock tolerance versus helical gear units, but helical reducers win on continuous-duty efficiency above 95% and lower unit cost. Selection hinges on torque density, duty cycle and ambient dust/moisture exposure.
Pillow block bearings handle light-to-medium radial shaft loads in fixed-centerline housings, while slewing ring bearings carry combined axial, radial, and moment loads in large-diameter slow-rotation joints. Selection hinges on load vector, diameter, RPM, and mounting geometry, not on a generic "st
Angular contact bearing FOB prices in 2026 sit in a US$1–20 per-piece band on Made-in-China listings, with precision/machine-tool grades climbing past US$50 once contact angle, tolerance class and cage material are specified.
Retaining rings span US$0.05–US$15.00 list-price per piece on 2026-07-01, with carbon-steel DIN 6799/471 external circlips under US$0.30 and OEM-spec beryllium-copper rings up to US$15.00 at 1-pc MOQ.
Timing pulleys for 2026 industrial and automotive use cluster around US$1-50 per piece FOB China, with steel MXL/XL/HTD types at US$1-10 and precision aluminum GT2/HTD5M runs at US$3-20; cost levers are material, tooth profile, MOQ and surface treatment.
Timing pulleys in 2026 sit in two distinct lanes: small-batch deflection/guide idlers around US$1-15 per piece and mid-volume custom HTD/MLT/GT synchronous wheels at US$1.50-15 OEM, with steel vs plastic, tooth profile and MOQ driving the spec.
Flat belts span stainless automation drives, rubber conveyor carcasses and PU timing/poly-V hybrids; spec the drive by load, speed, centre distance, environment and pulley diameter before pricing on Made-in-China or DYMCO channels.
A fluid coupling is a hydrodynamic torque-transmitting device with no mechanical connection between input and output shafts. Selection pivots on five hard gates: service factor, slip, thermal rating, input speed, and coupling-vs-coupler-vs-torque-converter distinction.
Planetary reducers in 2026 span 1–5 Nm coaxial units up to industrial 10–20 Nm gearheads, with 170 manufacturers and 1,127 listings on DirectIndustry; the buying decision sits on ratio range, backlash, radial/axial load, lubrication and IP rating.
Ball bearing sizing hinges on six gates: bore × series, dynamic load rating C, limiting speed n·dm, tolerance class (ABEC-1/3/5/7), lubrication regime, and seal/closure type — pick the bearing last, not first.
Angular contact bearings buy on contact angle (15°/25°/40°), bore, cage material, and pair-mounting logic; 2026 wholesale FOB ranges span US$0.78 to US$135.70 per piece, with single-row 7019 series from Chinese audited suppliers at 1000-piece MOQ.
MS16626B external inverted tapered-section retaining rings are still the dominant mil-spec for high-vibration shaft retention in 2026, with MISUMI configurable carbon-steel and 302/316 stainless variants covering most industrial buys.
RV reducers deliver single-axis precision under 1 arc-minute backlash for robot joint duty, while slewing drives integrate a worm or planetary gear set with a slewing ring bearing to handle 360° rotation, axial, radial and overturning loads in one bolted package.
Industrial gearbox FOB-China prices span US$50–500 per piece for helical-bevel K/H/B series reducers in 2026, with agricultural mower gearboxes at US$75–1,500 and harmonic-drive automation units near US$265, driven by frame size, ratio, torque class and material selection.
Linear guide selection hinges on six engineering gates — load capacity, accuracy grade, travel length, environment, lubrication, and life — applied before any model code is locked. Most RFQ rejections trace back to skipped accuracy and life checks, not to brand.
Ball splines for 2026 procurement run 6-50 mm shaft diameter across N/H/P accuracy grades with solid or hollow shafts, priced in Taiwan/China OEM catalogues and 8483.40 HS code.
Ball spline unit price typically spans US$80-3,500 per shaft as of June 2026, with 80-90% of total cost driven by nut/spline count, diameter, stroke and accuracy grade rather than the raw shaft alone.
Self-aligning bearing FOB prices span roughly CNY 5 to CNY 150+ in July 2026 depending on type, bore, cage and material; chrome-steel double-row ball units dominate, polymer and stainless variants carry 2-5x premiums.
Silent chain (inverted-tooth) drives deliver positive, no-slip power transmission with high torque density and low noise, suiting 2026 spec work where timing, lubrication-free service or harsh environments rule out roller chain. This guide covers types, ISO 606 grouping, pitch selection, lubrication
Universal joint buying decisions in 2026 turn on three verifiable levers: series (1310/1410/1480/1550/1610/1710/1810/1820/1880/7260), bore fit, and greasable vs non-greasable design. Spot prices span $13.88 (TRW 20191) to $42.65 (Moog 246/6GPB46) per retail SKU.
Gear couplings transmit torque between misaligned shafts in cranes, rolling mills and gearbox lines; 2026 buying centres on GICL/GIICL/WGP/WGC series, 42CrMo vs 40Cr hubs, NBR seals and API 671 / AGMA alignment limits.
Shaft collars locate components axially on shafts via set-screw or clamping grip, while spring washers maintain bolt preload under vibration — two distinct fastening categories with non-overlapping load cases.
For 2026 procurement, ball screws span US$1-10/piece for Chinese BK/BF end-supports and Hiwin-format catalogue items, with 345 mm stroke, preloaded single-carriage units such as Thomson 2HB20-150752 marking the precision end of the market. Spec the screw by lead accuracy grade, dynamic
Roller bearings in 2026 split cleanly into four procurement paths — tapered, cylindrical, spherical and needle — with FOB China bands of US$0.30–150 per piece, ABEC-1 through P2 precision classes, and 52100 chrome-steel vs case-hardened alloy as the dominant material lever.
Slewing drives for 2026 spec: worm-gear units from 3"–25" shaft diameter, hydraulic or SE motor input, holding-torque classes split into WEA (heavy, curved-tooth, medium speed) and SE (light/medium vertical-load solar tracker). Confirm load case, IP, ratio, and backlash gate before RFQ.
Lock nuts and retaining rings both fight back-loosening on a shaft, but they solve different problems: a lock nut clamps the threads of a fastener (axial preload on a threaded joint), while a retaining ring sits in a groove and axially captures a part on a shaft or in a bore (no threads involved). P
Conveyor chain selection in 2026 hinges on three measurable gates: pitch-to-shaft ratio, operating load (kN or N/m) and environment (corrosion, temperature, food contact). This guide maps chain type, material, attachment and certification gates to typical 2026 European industrial conveyor applicatio
Ball screw linear actuators typically deliver positional accuracy of 50 microns per 300mm with repeatability under 5 microns, while integrated ball-screw stages reach 3,200 mm/s and 13.76 kN load. Spec gate: stroke, lead, load, IP class.
Industrial universal joint (U-joint) FOB China prices span roughly US$0.86 for stamped economy 20Cr crosses to US$1.50–6.00 for GUM-71/GUT-11 grade forgings, while branded aftermarket assemblies such as Moog 264 list near US$24.99 retail; the dominant 2026 cost levers are material grade, forging vs
Spherical plain bearings are sliding-contact joints that handle misalignment plus combined radial/axial load, with steel-on-steel MoS2, PTFE-liner, and rod-end variants dominating 2026 sourcing. Specifying by sliding-contact surface, load direction, maintenance regime and ISO 12240-1 geometry is the
Belt tensioner selection hinges on four spec gates — drive type, OEM-equivalent part number, pulley diameter/width, and spring preload — with current market listings ranging from US $40 used assemblies to US $219+ new OEM units on eBay as of mid-2025.
Flat belt FOB pricing on major Chinese B2B platforms clusters between $2.00 and $8.78 per square meter at 100 m² MOQ as of June 2026, with urethane flat belts and rubber endless cords forming two distinct cost tiers driven by material, width and reinforcement.
Slewing drive selection hinges on five engineering gates: output torque, axial/radial load, gear ratio, IP rating, and mounting geometry. Specifying all five before RFQ eliminates ~80% of field failures and prevents costly over- or under-sizing.
Self-aligning bearings are double-row units that compensate 1.5°–3° of static shaft misalignment, with self-aligning ball versions for light loads and spherical roller variants for heavy shock loads above 100 kN.
Jaw couplings in 2026 span 11 Nm to 161,003 Nm torque across 85 listed OEM series; selection hinges on spider Shore hardness, bore fit, and contamination class, not on price tier.
Hybrid ceramic deep-groove ball bearings (Si3N4 balls, steel races) sit in the US$0.50-1.99/piece MOQ-1 band on China-made-in-china listings as of 2026-06-22; full-ceramic ZrO2 variants from custom-OEM factories price 5-20x higher.
Self-aligning bearings use a two-row rolling-element geometry to absorb shaft misalignment of typically 1.5–3°, while spherical plain bearings rely on an inner-outer race sliding pair to deliver oscillatory motion up to ±30° with maintenance-lubricated or self-lubricating PTFE liners.
Pillow block bearing prices in mid-2026 cluster between US $1.50 and US $30 per unit ex-works, with insert-mounted UCP/UCF/UCFL 205-206 series in 12-30 mm bores dominating the catalogue; landed cost is driven by housing material, insert grade and bore size, not by brand.
DIN 127 / JIS B1251 spring washers in 70C carbon steel and SUS304/SUS316 stainless, sized M3 to M36 (No.6 to 1-1/2"), remain the dominant split-lock washer spec for general bolt fastening, with Chinese tooling-machinery lines like the JP-320-3 driving sub-cent OEM unit cost in 2026.
Slewing ring bearings and roller bearings are distinct bearing families: slewing rings handle combined axial, radial and moment loads in large-diameter slow-rotation platforms, while standard roller bearings serve high-speed, small-bore shafts. Specification paths, load envelopes and supplier sourci
Timing pulley selection in 2026 is driven by pitch standard (MXL/XL/L/H/XH/XXH/T2.5-T20/AT3-AT20), tooth count, bore tolerance and material, not by diameter alone. Most stock OEMs ship 12-18 day lead time across 49+ SKU configurations.
Spring washer selection hinges on four lockable spec gates: load-deflection rate, free height vs working height, material grade (DIN 1.4310 / 51CrV4 / 65Mn), and corrosion class. Specifying the wrong gate costs 20-40% in premature fastener loosening on vibrating assemblies.
Planetary reducer 2026 price guide covers 170 manufacturers and 1,127 models on DirectIndustry; stage-1 helical-planetary PGFR90 units list around USD 90-250, stage-2 PGFR90 units run USD 220-700, while low-backlash precision gearheads commonly exceed USD 1,500 at the 90-115 mm frame band.
Tapered roller bearing selection hinges on six gates — load type (radial/combined), basic dynamic load rating (C), speed limit n×dm, ISO tolerance class, mounting arrangement — with single-row TS metric as the default and double-row TDO/TDI reserved for heavy combined loads.
Jaw couplings and fluid couplings solve different problems: jaw couplings transmit torque between two aligned shafts with a resilient elastomer spider, while fluid couplings transmit torque through a hydraulic working fluid between an impeller and runner for soft-start, overload-limited drive servic
Slewing drives and worm gear reducers both transmit power through a worm-and-wheel mesh, but slewing drives integrate a worm gearbox with a slewing bearing into a single rotary axis assembly rated for tilting and overturning loads, while worm gear reducers are standalone right-angle speed/torque con
Shaft collars in 2026 are specified by bore diameter, material (carbon steel, stainless 303/316, aluminium, acetal), and clamping style (one-piece set-screw vs two-piece clamp). Misaligned priorities cause slip, galling, or shaft damage.
Timing pulleys set the gear ratio on a synchronous drive; belt tensioners set the load that keeps the timing belt engaged. Specifying both correctly is a 4-gate problem: pitch, OD/width, belt length, and tensioner force window.
Conveyor chain and flat belt are the two workhorse transport mediums in 2026: chain excels at heavy load, incline and high-temperature service; flat belt wins on long distance, food-grade and low-noise duty. Spec selection turns on load per meter, incline angle, environment and maintenance access.
Ball bearing buying in 2026 is dominated by angular-contact and deep-groove 6000-series units, with Chinese distributors quoting roughly US$1–20/piece MOQ 1 and authorized brand channels (e.g. SKF Platinum) holding a separate price/lead-time tier. Match bearing type to load, speed, misalig
Disc spring washers scored 1-out-of-5 reusability and "High" lifetime cost in Nord-Lock's May 2026 bolt-securing comparison, while dedicated locking assemblies remain the spec default for safety-critical bolted joints.
Ball screw selection is a load- and life-driven engineering exercise, not a catalogue browse: shaft buckling, axial load, DN value, lead accuracy and lubrication class gate the model code before RFQ in 2026.
Locking assemblies deliver full 360° friction-locked shaft-hub contact with zero backlash, while shaft keys rely on localized positive engagement; selection hinges on torque density, reversibility, and shaft-step tolerance.
Linear module FOB China price ranges from US$500 to US$1,800 per unit for compact ball-screw stages with 150 kg horizontal / 55 kg vertical payload and ±0.01 mm repeatability, driven by stroke length, drive type, accuracy class, and payload.
Ball bearing list price in 2026 spans roughly US$0.50 for unbranded 6204 deep-groove units to US$800+ for stainless or ceramic hybrid equivalents, with size, tolerance class, seal configuration and material grade doing the heavy lifting on the invoice. As of 22 June 2026, 33 ball-bearing rail vendor
A jaw coupling is one specific sub-type of flexible shaft coupling, not a competing category. The engineering choice is between a jaw (spider) coupling and other shaft-coupling families: gear, disc, fluid, universal-joint, and rigid clamp couplers.
Ball spline selection hinges on five engineering gates — shaft diameter class, static/dynamic torque rating, shaft length envelope, radial-load capacity, and mounting style — with the IKO/Nippon Thompson line shipping shaft diameters from 5 mm to 25+ mm and stock lengths of 20, 100 and 150 mm.
Steel tapered roller bearings carry combined radial + axial load from 17 mm to 230 mm bore at €7.68–€73 list price; full-ceramic Si3N4 deep-groove ball bearings list US$0.29–25.00 and are limited to radial-only, light-duty service.
Linear module buying in 2026 is dominated by ball-screw, belt-drive and roller-screw stages in widths from 50 mm to 210 mm, with stroke extending past 1 m, repeatability at ±0.01 mm on premium units, and IP-rated clean-room bodies costing roughly USD 200–3,500 FOB depending on size and lead-screw ty
Selecting a slewing ring bearing in 2026 hinges on five lockable spec gates: load case (axial/radial/moment), rolling-element type, gear integration, diameter series and ISO 9001-documented supply. Crossed-roller, single-row ball and triple-row roller variants serve distinct load profiles.
Industrial hydraulic shock absorbers in the KMA20-16 family list on DirectIndustry at indicative bands of US$83–98 per set MOQ for mid-volume Chinese OEM supply, while aftermarket automotive units sit £25–55 retail and motorcycle dampers trade at sub-US$10 factory FOB at 300-piece MOQ.
Industrial shock absorbers absorb kinetic energy and convert it to heat via hydraulic orificing, while gear couplings transmit torque between shafts with zero backlash. They solve different problems: vibration damping versus positive-drive shaft connection.
Slewing ring bearings in 2026 are ordered by bore diameter (100–1800 mm), rolling element (ball / roller / crossed roller), gear form (internal / external / none) and precision class (P0–P4 or ABEC 1–7). Match load case first, then size and gear.
Spring washer FOB pricing in mid-2026 sits between US$0.03 and US$0.30 per piece at 1,000-piece MOQ for stainless-steel flat gaskets from Chinese wholesalers, with cost driven mainly by material grade, type (helical split, Belleville DIN 2093 disc, curved) and order volume.
Fluid couplings in 2026 are specified by torque capacity, application class and start duty, not by brand. ESC-series units for pumps, fans and conveyors dominate the variable-speed segment, while PPR/couplings and profile couplings cover low-torque and pipe-fitting duty.
Universal joints and disc couplings solve different misalignment problems: the universal joint handles large angular offsets and torque swings to 250,000 Nm, while the disc coupling manages small parallel/angular misalignment at high speed with zero backlash and no lubrication.
RV reducer selection hinges on five gates — rated torque, ratio, backlash, tilting moment and IP class — that lock the unit before RFQ. RV reducers beat harmonic drives on shock load and beat planetary stages on single-stage ratio density for heavy-payload robotics and CNC indexers.