Gate valves provide media isolation with minimal flow restriction, and rising internal pressure increases the sealing load on the bonnet in a pressure-seal design.
Selection depends on design pressure, operating temperature, media, pressure class, seat leakage, actuator duty, and piping arrangement across fossil, combined-cycle, nuclear, solar-thermal, and hydroelectric plants [S1][S2].
Gate Valve Duty in Power Plant Steam and Water Systems
A gate valve should normally be operated only fully open or fully closed. Its disc or wedge obstructs the flow path to provide isolation with less restriction than a throttling valve, so using it as a control valve can produce damaging velocity and erosion conditions [S4][S5].
Power-plant gate-valve applications include steam isolation, boiler feedwater, natural gas, cooling-water circulation, and water treatment. Gate valves are used for isolation rather than throttling and should be operated fully open or fully closed.
For a steam or water line, document the design pressure, maximum metal temperature, normal operating pressure, allowable pressure-temperature limits, and required seat leakage before selecting a body and trim material. Selecting a gate valve requires consideration of the station's pressure, temperature, and media conditions and of the appropriate valve configuration and materials.
Bolted Bonnet Versus Pressure Seal Architecture
Power-plant gate valves are available in bolted-bonnet and pressure-seal designs. The pressure-seal bonnet uses internal pressure to increase sealing load as system pressure rises, reducing the risk of joint leakage.
The choice depends on disc geometry, thermal movement, seat geometry, and the plant's operating envelope rather than pressure class alone.
Detailed gate valve design terminology helps procurement teams distinguish disc, wedge, bonnet, seat, and closure concepts in the specification.
Pressure, Temperature, and Material Limits
Power-generation piping can combine high pressure, elevated temperature, thermal cycling, and rapidly changing flow conditions. Combined-cycle plants impose particularly severe starts, accelerations, and thermal transients, while coal-fired plants place greater emphasis on steam pressure and temperature [S2].
These designations identify design families, but the purchase specification must still define the applicable class, size range, materials, seating, stem, bonnet, seals, actuator, and testing requirements.
Do not assign a pressure-temperature limit from the standard code alone. The selected body, bonnet, stem, seat, disc, bolting, and gasket materials must be compatible with the maximum design pressure, design temperature, and expected cycling. For high-temperature services, verify seat expansion, body-to-bonnet differential expansion, stem strength, and actuator clearances at the closed position.
Comparison With Alternative Isolation and Control Valves
Gate valves and globe valves are classified as isolation valves, and power-plant valves perform different roles within the plant. Gate valves provide straight-through isolation, globe valves provide throttling and flow regulation, and check valves prevent reverse flow [S1].
The mainstream gate valve is a poor choice for variable steam flow because partial opening creates high velocity, erosion, vibration, and unstable torque. Globe valves are preferred when gradual flow control is required, but they introduce greater pressure drop and are less suitable for unrestricted full-flow isolation. Check valves are automatic protective devices rather than manually operated isolation points.
Seat Leakage, Actuator, and Maintenance Requirements
Power-plant valve configurations must accommodate thermal transients and cyclic operating conditions. These are mechanical and process risks, not merely procurement deviations.
For fugitive-emissions control, one manufacturer describes converting valves to house API 624 packing and reducing leakage to 100 ppm [S1]. Specify the applicable packing arrangement, bonnet design, stem material, actuator torque, and tested leakage class rather than relying on a generic low-emission label.
The actuator must deliver the required seating torque at minimum differential pressure without overstressing the stem or gearbox. Include maximum allowable operating pressure, fluid density, friction assumptions, travel time, manual override, limit switches, and fail action. Electric, pneumatic, and hydraulic operators each have distinct failure behavior, so the required fail position should be established before the actuator is selected.
Application Fit by Plant Type
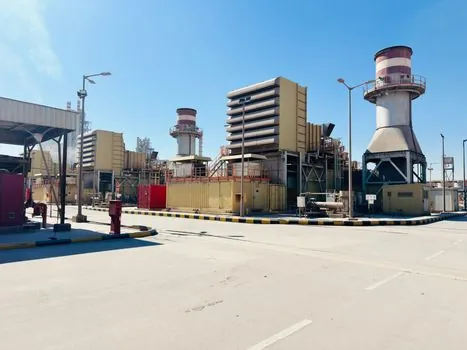
Fossil, natural-gas, combined-cycle, nuclear, and solar-thermal stations require different pressure, temperature, and media conditions, so a plant-wide valve schedule based on one generic gate-valve specification will not be reliable [S1]. Combined-cycle applications also expose valves to rapid thermal transients and higher gas-turbine start frequencies [S2].
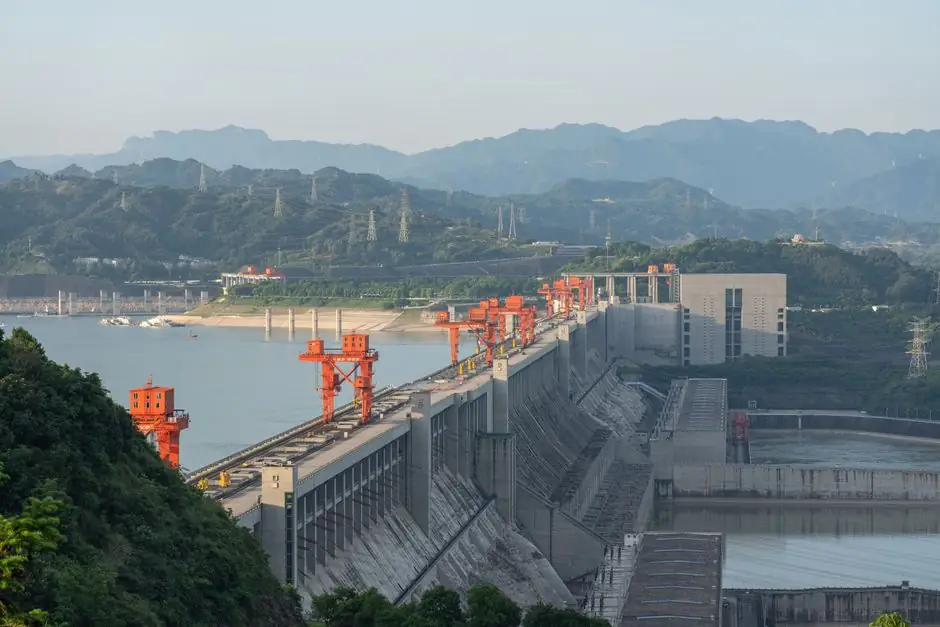
Hydroelectric plants use gate valves in the penstock, the pipeline carrying reservoir water to the turbine [S9]. Nuclear duties require project-specific compliance, material traceability, testing, and documentation beyond a commercial power-plant valve datasheet. Solar-thermal systems can include high-temperature steam or heat-transfer service, requiring validated material limits rather than generic water-service ratings.
A knife gate valve may suit certain bulk-material or high-cycle applications, but the standard power-plant gate-valve family is the better starting point for pressurized steam and liquid pipelines when tight shutoff, low pressure loss, and conventional operating maintenance are required.
Procurement Specification and Acceptance Tests
A complete power-generation gate-valve data sheet should identify valve type, size and pressure class, flow direction, design and operating pressure, design temperature, body and trim materials, disc configuration, seat type, stem arrangement, bonnet type, end connection, actuator specification, and required coating [S1][S4].
Inspection and testing should cover shell strength, seat tightness, operation, and documentation appropriate to the service and governing procurement specification. For pressure-seal designs, include a clear requirement that the bonnet joint remain leak tight at the specified shutoff pressure. For high-temperature service, request evidence that the seat, disc, stem, and bonnet materials are suitable for the stated temperature.
Before shortlist approval, verify three documents: the valve data sheet, the approved material list, and the piping or system P&ID. Any disagreement between the data sheet and P&ID, such as an unspecified pressure class or inconsistent direction of flow, should be resolved before fabrication. For steam-throttling misuse and its mechanical consequences, see why a gate valve fails at steam throttling.
The shortlist logic is straightforward: use a bolted-bonnet gate valve below ANSI Class 600 where its pressure and temperature limits fit, move to a pressure-seal design above 500 psi, select parallel-disc or flexible-wedge geometry against the thermal and seat-loading conditions, and reject any gate valve specified for throttling.