The torque settings of Beta Power Engineering overload protection clutches are accurate to ±10% even after repeated tripping.
A torque-limiting device can absorb overload before the resulting energy is transmitted into critical components.
Clutch trip torque is a system setting, not a catalog guess
Depending on the model and its intended function, a torque-limiting clutch will either slip or completely disengage during a torque overload.
Start by separating three values: normal running torque, maximum expected working torque, and the overload condition that the clutch is intended to interrupt. The trip point belongs above maximum expected working torque but below the load level capable of damaging the gearbox, shafts, sprockets, bearings, or chain. Without that separation, a clutch set too low becomes an operating nuisance, while a clutch set too high becomes ineffective protection.
For friction-based protection, spring pressure is adjusted to establish the torque at which the limiter slips [S8]. Available devices may instead slip or fully disengage, so the required response must be defined before a model is selected [S6]. This distinction affects whether the conveyor can restart automatically after the obstruction is removed.
Choose slip or disengagement from the restart requirement
A friction torque limiter slips at its overload threshold, while a disengaging design separates the drive train; torque-limiting clutches can be configured for either behavior [S6].
The comparison below defines the engineering decision before the trip torque is calculated.
For a chain conveyor using roller chain, the clutch or limiter should be compatible with the chain, sprocket, coupling, and shaft arrangement. Available overload clutches can be supplied with roller chain or an elastomeric coupling [S1], while heavy-duty catalogue families include torque limiters intended for conveyor, compressor, pump, and rolling-mill service [S4][S5].
Use the clutch setting to protect every drivetrain element
A conveyor jam creates a rapid torque spike that transfers into gears, bearings, shafts, and chain if no overload device yields first [S5]. This is why the clutch trip torque should be evaluated against the weakest credible load path rather than against motor rating alone.
Four checks should frame the calculation. First, compare the proposed trip torque with the drive system’s normal starting and running torque. Second, identify the rated capacity of the gearbox, shafts, sprockets, and bearings. Third, account for the conveyor configuration, including incline, loading, and friction. Fourth, establish whether the protection should stop only the chain or isolate the motor and gearbox as well.
For an incline transfer, the motor-selection and starting-torque assumptions should be coordinated with the clutch setting rather than handled separately. The related engineering sequence for sizing chain conveyor motors for incline transfer provides a useful load and starting framework. In all cases, the clutch setting remains a protection threshold, not an operating output target.
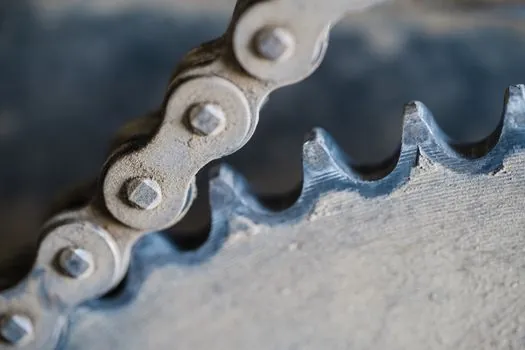
The physical transmission path matters because roller chain, chain conveyor, and chain-conveyor drive components do not all share the same overload behavior. A properly placed limiter should isolate the load before excessive torque reaches the chain and sprocket set.
Adjust the setting with a controlled commissioning procedure
Some torque overload devices leave the factory at their minimum torque value, so the installed condition must be checked before startup [S7]. Adjustment should follow the manufacturer’s sequence, with the drive isolated from hazardous energy and the indicator checked before the clutch is exposed to operating load.
Commissioning should proceed through four stages. First, verify the model, coupling or chain interface, shaft arrangement, and mechanism condition. Second, confirm the mechanism’s minimum and maximum adjustment range. Third, set the device below the calculated trip point and complete a controlled test under the anticipated load. Fourth, record the final indicator position, test load, observed slip or disengagement behavior, and reset procedure.
Beta Power Engineering states that its overload protection clutches have torque settings accurate to ±10% even after repeated tripping. That tolerance must still be included when selecting the final threshold because a nominal setting is not the same as a measured release point. Mark the approved setting and make it part of maintenance inspection, particularly after any change to motor, reducer, chain pitch, conveyor slope, or material loading.
Use built-in sensing to confirm the actual trip state
Overload-clutch product families include mechanical and non-contact proximity-switch options, including a SIKUMAT proximity switch for detecting limiter state [S4]. Such sensing can link the trip event to a stop command, an alarm, or a controlled restart sequence.
The sensing arrangement should distinguish normal engagement from slip or disengagement and should be tested with the machine stationary as well as under the controlled overload test. For a non-contact switch, commissioning must include target position, sensing distance specified by the manufacturer, and response to the actuator’s actual movement. For a mechanical switch, inspection must cover contact condition and actuator travel.
The associated clutch brake may be relevant when the application combines overload release with controlled stopping or holding. Its role must remain separate from the clutch’s mechanical overload threshold: the clutch protects the drive train, while the brake controls stopping or holding functions.
Match the reset method to the failure severity
An overload event should not be treated as a routine reset. A friction limiter may slip and re-engage automatically, while a disengaging clutch remains separated until the obstruction is removed and the machine is checked [S3][S5]. The operating procedure must state whether an immediate restart is permitted after a known, minor obstruction or whether inspection is mandatory.
Three failure modes deserve specific procedures. A jam caused by loose material may permit clearing, inspection, and controlled restart. A jam involving a bearing, sprocket, or chain seizure requires isolation and mechanical inspection. A trip caused by an incorrect clutch setting, damaged mechanism, or unexplained load requires corrective action before the conveyor returns to production.
Automatic re-engagement is not itself proof that the fault has been corrected. Tolerance rings act as self-resetting slip devices and can re-engage after an overload [S5], but the underlying restraint can remain. A reset event should therefore trigger an alarm record and a controlled restart rather than an unrestricted continuation of production.
Specify the clutch with the complete conveyor package
A purchasable specification needs more than a rated torque. It should identify the conveyor drive arrangement, chain or coupling connection, clutch model family, required response to overload, adjustment range, torque-setting tolerance, proximity-sensing option, and reset procedure [S1][S4][S6].
The specification should also identify the calculation inputs: normal running torque, maximum expected working torque, starting torque, incline or friction contribution, selected drivetrain service factor, and the lowest credible component damage threshold. Where calculations conflict with the catalogue range, the clutch is unsuitable for the installation and the drive train must be resized rather than the protection threshold forced beyond its limits.
Supplier details still require engineering verification. One overload-clutch manufacturer specifies tripping torque within ±10% after repeated trips and offers roller-chain or elastomeric-coupling connections [S1]. Another catalogue separates friction torque limiters, force limiters, ratcheting designs, and disengaging designs by model series [S4]. These are selection inputs, not permission to copy a setting from another conveyor.
The traceable commissioning record should include the calculated target, permitted adjustment range, final set value, observed trip behavior, reset result, and any post-trip inspection. If the first trial trip occurs at an unexpected point, stop the test and determine whether the cause lies in the setting, coupling slip, shaft torque, load distribution, or a damaged component before raising the threshold.
The next engineering action is to produce a one-page clutch setting sheet containing the four torque values, selected clutch series, allowable adjustment range, sensing arrangement, and reset rule, then validate the installed unit with a controlled overload trial.