
Robotic vs Mechanical Case Packer Cycle Rate
Mechanical case packers suit stable, high-volume runs, while robotic systems favor frequent SKU changes despite lower single-case speeds.
Read →Industry News · Category
Mechanical case packers suit stable, high-volume runs, while robotic systems favor frequent SKU changes despite lower single-case speeds.
Read →
Manual and automated packing should be compared using total operating cost, required flexibility and sustained output, with machine payback depending on volume, staffing, changeovers, maintenance and the value of capacity.
Case packer changeover-part cost depends on mechanical adjustments, recipe-driven controls, reusable tooling, and line integration, not just the replacement-part list.
Case packing machine ratings span 1 to over 75 cases per minute, but actual output depends on product handling, case size, and uptime.
Choose a case checkweigher rated to 25 kg, with verified case dimensions, stable conveying, and a reject system sized for the line. Published heavy-duty models offer 0.05–25 kg ranges and 1 g resolution.
An automatic carton erecting machine can produce 10–40 cases/minute versus 2–4 cases/minute manually, cutting labor cost when volume supports the investment.
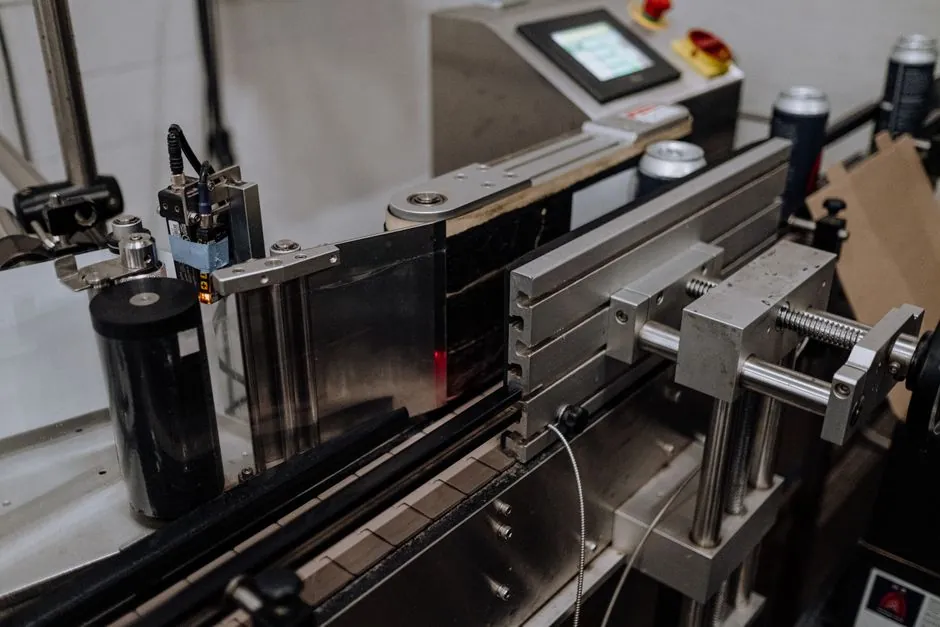
Sequence the carton erector before the filler, then buffer and inspect cases between stages to prevent product backpressure and carton damage.

The CE 20N automatic carton erector has an output of 12 boxes per minute, while specialized high-speed cartoners can reach 400 cartons per minute.
Set hot-melt glue open time above the flap-closing cycle, then verify press time against bond strength; longer open time aids adjustment but can weaken throughput.
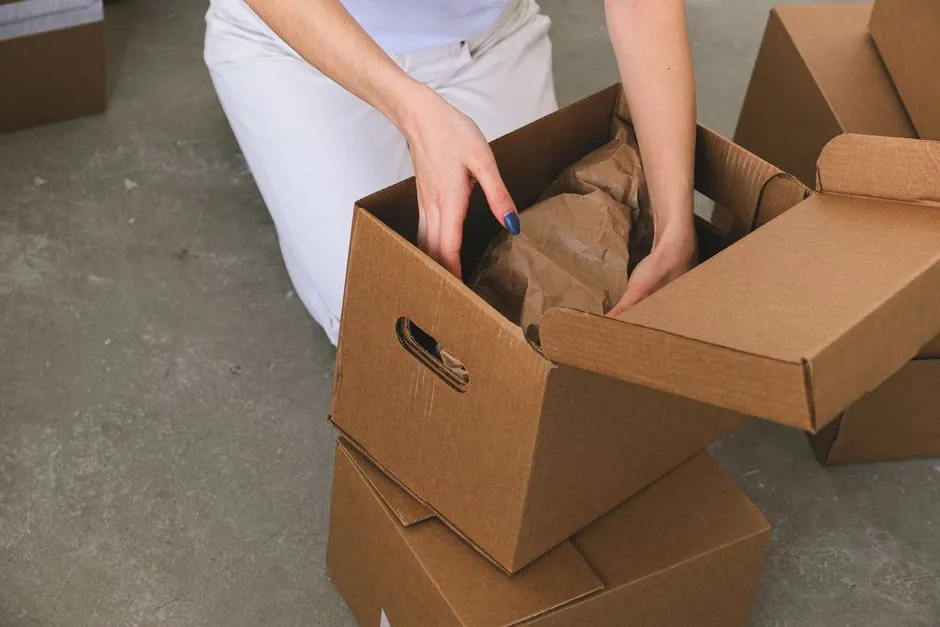
Case erectors pick up flat cardboard blanks, shape and erect them, fold the bottom flaps, and seal those flaps with tape or glue to prepare the boxes for product loading.
A 300-blank magazine can sustain 20 CPM for 15 minutes, so uninterrupted carton forming depends on board grade, feed reliability, and reload time.
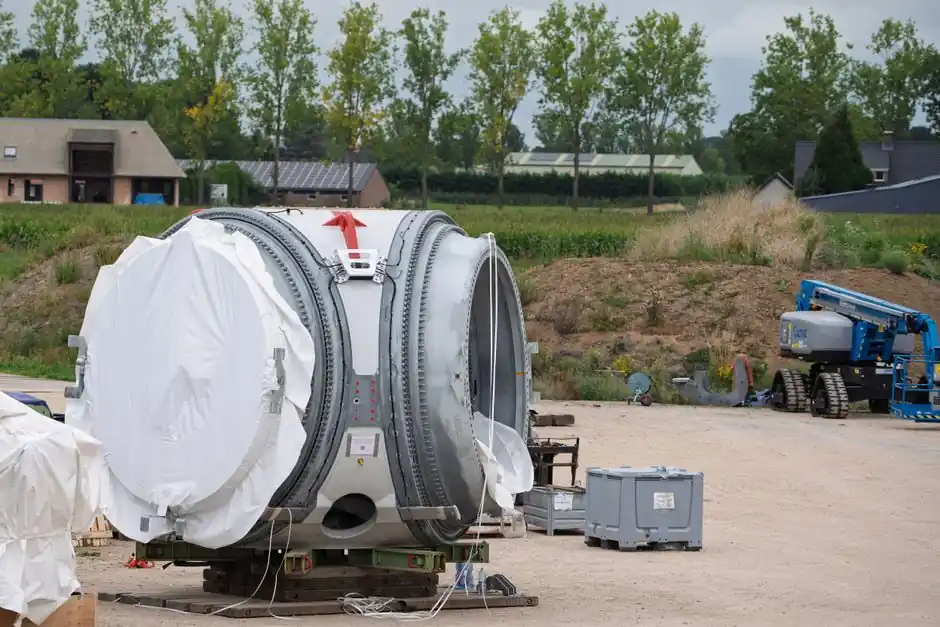
Choose a wood crate for heavy or irregular machinery parts requiring multi-ton support, blocking, and weather protection; use a carton box for lighter, repeatable loads.
Choose single-use cartons for low-return flows and reusable turnover boxes for closed-loop transport. Total cost depends on cycles, loss rate, reverse logistics, and cleaning.
Choose corrugated pallet boxes for boxed or moisture-sensitive goods; choose FIBC bulk bags for dry, flowable granules sold in high volumes.
Choose recycled board for cost and fiber reduction; choose virgin kraft for peak strength, moisture resistance, cleanliness, and premium print.
Specify cartons by internal L × W × D for product fit and external L × W × D for freight, storage, and pallet planning.
Machine-grade cartons should hold length and width within ±2 mm, use 2 mm flap clearances, and maintain squared panel dimensions for reliable automatic case packing.
Lightweight high-performance liner board can cut corrugated costs through less paper, freight, storage, and handling, provided the box still passes compression and transit tests.
Compare corrugated carton cost per unit by calculating board, labor, freight, and damage costs. Single wall suits light loads; double wall protects heavy or fragile loads.
Calculate the bottom-carton BCT from stack load and duration, apply a 3:1 factor, then verify the design against pallet height and humidity.

A 200# Mullen rating measures 200 psi of face-burst strength, making it suitable for puncture resistance, while ECT governs stacked-load performance.
Store corrugated cartons in dry conditions and protect them from moisture, condensation, and sunlight to help preserve their strength and condition.
Use cap-then-label sequencing for most stable liquid bottles: the filled container reaches final weight and cap geometry before label application.
Sequence filling before capping, verify closure quality, then label only after capped containers pass inspection. Use synchronized conveyors and controls to prevent filling-to-capping accumulation.
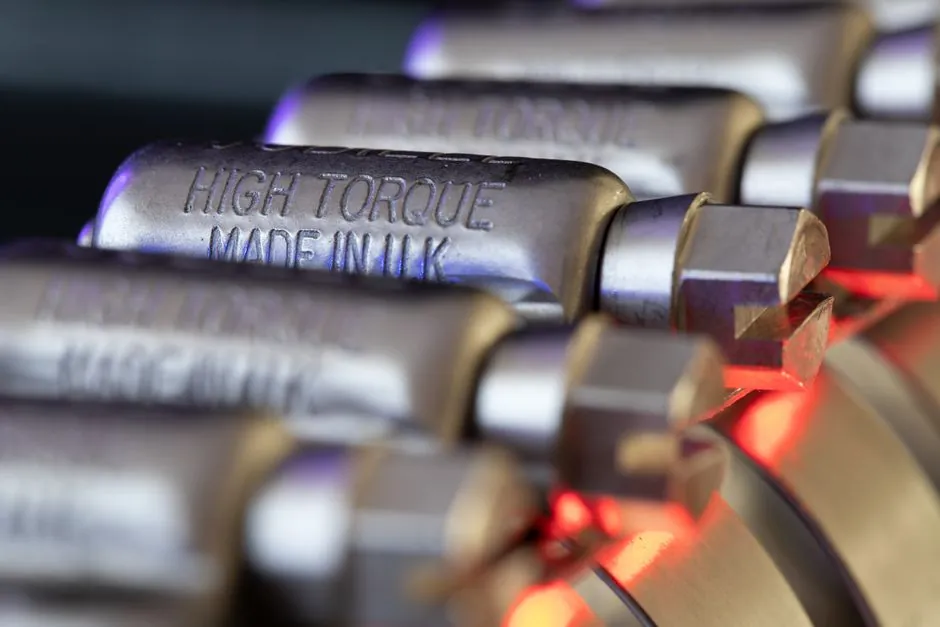
Set capping torque from the closure and bottle-finish specification, then verify it with calibrated application and 24-hour removal-torque tests.

High-volume cappers range from 60 to 200 caps per minute, but the correct specification depends on closure geometry, torque, feeding, and line synchronization.
Set induction cap-sealer power by liner material and thickness, not a universal wattage. Start low, hold sealing time and air gap constant, then increase power in 1–2% steps.
Choose foil liner thickness by testing 40–80 µm foil structures against container material, sealing film, coil power, and line speed before production release.
Inventory changeover parts by cap diameter, bottle geometry, closure type, and torque program, with 15–30 minute changeovers as a realistic planning range.
Choose induction sealing for leak-resistant inner seals; choose capping with bands or sleeves for visible closure integrity and branded tamper evidence.
Multi-head capping-machine cost per head depends on speed, closure type, materials, controls, and line integration. Published prices support single-head benchmarks, not direct per-head quotes.

Radio shuttle lanes can run FIFO or LIFO, with mode selected in shuttle software per lane or SKU. FIFO requires controlled pallet positioning and sequence logic.
Oxygen reduction can prevent ignition in an AS/RS high-bay, but it should complement an approved sprinkler design rather than replace it without code review.
Yes. An order picker can be retrofitted with barcode scanning by adding location labels, mobile scanners, and WMS or ERP integration.
AMRs can move between facilities, but the robot may transfer faster than its software, maps, workflows, and integrations.
A VLM can store frozen goods at -20°C only with a manufacturer-qualified cold-store package, insulation, refrigeration, and low-temperature-rated controls.
Yes. A truck scale can be relocated if the deck, load cells, wiring, foundation, drainage, and legal-for-trade certification are inspected and recertified at the new site.
A stacker crane can be retrofitted with a new load-handling device, but compatibility, load geometry, controls, and safety must be verified before installation.

A shuttle system uses deep lanes and rails, and its suitability depends on facility conditions and planning decisions.
A mobile manipulator AMR can pick individual items when its arm, vision system, gripper, and navigation work as one coordinated system.
At 150°C, clinker can be conveyed by a belt bucket elevator only with a heat-rated belt, hot-resistant buckets and verified temperature ratings.
Yes, a washdown-rated bench scale can withstand routine wet cleaning, but only when its IP rating, sealing, surface, and cleaning limits match the installation.
A capable USB webcam for camera-based obstacle detection costs ₹500–₹2,000, while entry-level LiDAR modules start around ₹8,000–₹12,000 for basic single-point units.
Use a cageless rigid HDPE IBC on an integrated 45 x 45-inch pallet for dense liquid storage, with 330-gallon capacity and stack limits set by the support system.
Pneumatic tanker unloading typically uses 0.15–0.25 MPa tank pressure, but material, piping, and receiving-silo conditions determine the final setting.
Densification and inflatable spout sealing improve bulk bag fill quality, while weighing capacity, throughput, and dust control determine the right system.
A bucket elevator fits compact 90-degree bulk lifts; a belt conveyor fits longer runs, and high-angle sandwich belts bridge moderate inclines.

A single-leg bucket elevator may reach 50 ft before intermediate support, but final spacing depends on load, casing, drive, shaft stiffness, and code requirements.

Place inspection doors at the head, boot, and intermediate casing to support safe bucket, belt, liner, pulley, and sprocket maintenance access.
Internal bucket legs reduce structural interference, while external legs simplify inspection. Choose by capacity, material abrasiveness, space, and maintenance access.

For a bucket elevator, use the inlet loading leg to meter material into the buckets and the discharge throat to control release at the head; the two functions require different geometry.

Full-load startup torque, not steady-state power, usually governs bucket elevator motor size. Verify drive torque, gearbox capacity, backstop performance, and starting method.

Budget $180–$350 per meter for a chain bucket elevator, then add structure, foundations, discharge systems, controls and erection for a realistic total.

Bucket elevator belt replacement costs less than rebuilding a complete leg, but belt-only work is justified only when the casing, boots, pulleys, buckets, and drive remain serviceable.
Use 12-gauge casing where specified, 6.4 mm boot liners on BE36–BE48 models, and wear liners for abrasive service, matched to measured impact and abrasion.
Size bucket-elevator relief panels from the calculated gas-generation rate, casing volume, and discharge path, not casing width alone.
Use widely spaced, high-speed buckets for free-flowing material; use closely spaced, lower-speed continuous buckets for sluggish, sticky, fragile, or abrasive material.
ECT grades stacking-related edge crush, Mullen grades burst resistance and BCT predicts compression performance of the finished box. The purchase spec should carry the number the distribution actually loads.
Use fanged elevator bolts for vibration-heavy bucket elevators and ordinary square-neck bolts for low-speed, light-duty service. Rivets suit permanent joints, not routine bucket maintenance.
Choose a vulcanized splice for permanent, high-tension service; choose mechanical fasteners for rapid field repairs and frequent belt changes.
Belt bucket elevators suit higher-speed, cleaner duties; chain systems favor abrasive, heavy, hot material despite lower speeds and greater maintenance.
Choose 50 mm tape for standard 2-inch case-erector heads and adequate panel coverage; choose 70 mm only after confirming head, roller, and application clearance.
Choose a split-tray sorter for high-speed, flat-drop polybag sorting, and a tilt-tray sorter for mixed, heavier, or irregular loads.
Choose a long-radius bend for general solids handling, a blind tee for abrasive wear control, and a vortex bend for constrained layouts where impact forces must be managed.
A binary-array CIJ printer can mark up to six lines or dense DataMatrix codes, but speed, nozzle architecture, and ink compatibility must be matched to the line.
IP69K washdown bench scales suit food plants exposed to high-pressure, high-temperature cleaning; IP66K or IP65 units fit less severe wet areas.
Choose a bench scale for parcels up to 500 lb and a truck scale for complete vehicles; match the instrument to the load, workflow and accuracy need.
Choose a bench scale for manual spot checks and a filling scale for continuous dosing, with capacity, readability, and throughput matched to the job.
Choose 304 stainless steel for wet or corrosive duty; choose painted steel for dry workspaces where corrosion resistance and washdown protection are unnecessary.
Use one single-point load cell for a compact bench platform; use multiple load cells for larger, higher-capacity structures requiring shared-load balance.
A 0.1 g bench scale is a practical choice for weighing and counting small parts, provided its capacity, minimum load and stated accuracy fit the job.
Choose a platform scale when an oversized load cannot fit safely on a bench scale. Match usable deck dimensions, capacity, access, and load arrangement.
For small parts, a counting scale should use at least 10 samples, with 100 preferred, while resolution must equal or better than one part’s weight.
Specify bench scales by safe overload margin, shock isolation, ingress rating, and alarm behavior, because a 150% load limit alone does not prevent accidental-load damage.
For Class II bench scales, use 20 d as the recommended minimum load when e is 0.001–0.05 g, and 50 d when e is at least 0.1 g.
IP65 bench scales are dust-tight and resist low-pressure water jets, but IP66–IP68 are better choices for intensive hose-down cleaning.
Bench-scale NTEP models cost about $300 more than comparable industrial-only models, but certification is required when price is determined by weight.
Basic bench scales cost less; data-logging models cost more because they add storage, interfaces, and records-management hardware.
Light-industrial bench scales span about 0.6–3000 kg; select by maximum load, minimum increment, platform, environment, and legal-for-trade needs.
Choose AC power for fixed, high-use bench weighing; choose battery power only when mobility or no outlet justifies added charging and battery-management duties.
Conveyor Pro SP belt chamber vacuum machines package food and non-food products continuously at up to 3 cycles/min and 40 m/min.
Calculate T1 and T2 from effective tension, pulley friction, and wrap angle, then size the take-up, motor, and belt against slip, sag, and service limits.
Steel cord conveyor belts carry a recommended safety factor of 6.67 to 7 against maximum working tension, while fabric/textile belts require roughly 8 to 10 under DIN 22101, with a documented splice efficiency gap of 90%+ for cord belts versus 70-80% for fabric plies driving the differential.
For fine powders, specify a screw conveyor when run is under 30 m, incline is steep, and full dust containment is required; pick a belt conveyor only for long, open, high-tonnage abrasive streams.
Belt conveyors typically consume 0.007-0.03 kWh per tonne-kilometre, with the belt itself driving 90% of total system energy use. A 9.03 kW drive moving 800 tph over 150 ft consumes 79,103 kWh/year, costing $7,910 at $0.10/kWh.
Rubber conveyor belt price per metre in 2026 spans roughly $25–$60/m for general-purpose PVC and rubber belts, climbing to $120/m or more for textile, steel-cord, or specialty constructions, while installed warehouse conveyor systems run $30–$2,000 per linear foot. Real landed cost is driven by carc
Battery-powered mobile robot wrappers (e.g. Robot S7, Handle It 3000) deliver 200–250 pallets per charge, wrap up to 30 loads/hour, and handle oversized/heavy loads beyond the 1,500–2,500 kg ceiling of rotary-table wrappers, making them the default for decentralized warehouses and unstable pallets a
Battery friction-weld strapping tools and manual tensioner-and-seal sets are the two endpoints of the PET/PP pallet-strapping decision: one tool, one button, no seals, higher unit cost; the other, two hand tools, separate buckles, lowest entry price. Pick the battery unit when daily volume or seal a
Ball transfer tables and roller conveyors solve different problems: pick balls for omnidirectional manual positioning, rollers for linear throughput. Use the 1/3 shortest-dimension rule for ball grid pitch and 5-ball minimum support for stable flat-bottom loads. Match equipment to flow geometry, not
Balanced weave belts and flat wire belts are two of the most common metal conveyor constructions, and the right pick depends on drive type, open area, load profile and temperature. Choose balanced weave for friction-driven, high-flex routes and flat wire for sprocket-driven, high-tension, drainage-h
For 25 kg open-mouth bagging, single-spout net-weigh lines run 450-900 bags/hour while twin-spout configurations reach 1,000-1,800 bags/hour. Choose single for runs under 600 bags/hour or frequent changeovers; twin pays off above 900 bags/hour with stable granules.
Baffle FIBCs hold a near-cubic shape when filled, while standard FIBCs bulge into a rounded profile, making baffle bags the default spec when warehouse or container stack height exceeds two layers. Industry guides now quantify the gain at up to 30% higher storage density and 3-4-high safe stacking,
AMR-based goods-to-person (G2P) retrieval and stacker-crane AS/RS compete on flexibility, density, and throughput per square meter. AMRs win when SKU counts exceed a few thousand and order profiles vary hourly, while stacker cranes still dominate at very high ceilings and single-digit-second cycle t
AMR-based robotic sortation can cut sorting footprints by 50–70% and deploy in under two weeks, while fixed conveyor sorter systems still dominate peak-hour throughput above roughly 10,000 parcels/hour per lane. The decision hinges on parcel mix, peak-to-average ratio, and order profile volatility,
AMRs and pallet shuttles solve different parts of the SKU velocity problem: shuttles dominate high-velocity deep-lane storage, AMRs handle the heterogeneous horizontal flow between dock, rack face, and production. Specs like 3,000 lb shuttle load, 80% single-deep density, and 99.5% inventory accurac
AMRs win on flexibility and variable order profiles; conveyor sorting lines win on sustained high throughput and fixed routing. Choose AMRs when SKU mix shifts weekly, choose conveyors when parcel volume is steady and lane counts are fixed.
Conveyor, lift, and tugger top modules are the three dominant AMR attachments, each defined by payload class, load transfer method, and aisle-width footprint. Selection hinges on whether the load is unitised, whether a fixed conveyor handoff exists, and whether the route is point-to-point or stop-an
AMRs typically deploy in 2-6 weeks without floor infrastructure, while AGVs take 8-16 weeks including path installation and commissioning for a new facility. For dynamic, high-mix operations, AMRs deliver faster go-live; for heavy, fixed-path, high-precision work, the AGV timeline still pays off.
Camera vs LiDAR alone is the wrong question for AMR collision avoidance: fusing a 2D/3D LiDAR with a camera lifts effective obstacle detection range by 1.94x and pushes per-decision accuracy above 94%, per 2024-2025 peer-reviewed and industry measurements.
Safety-rated LiDAR on autonomous mobile robots now spans 1.5 m to 75 m reach with FOVs from 90°×90° to full 360° hemispheres; single 2D safety scanners mount near 200 mm height and miss 100 mm underhangs, pushing fleets toward 3D LiDAR or ADAR.
Standard tote footprints (400×600 mm, 600×800 mm) are dimensionally compatible with current AMR decks in the 40–120 kg payload class, but only when the deck plan is matched to the tote plan and the chassis is sized for total installed load, not tote weight alone. Lift-equipped AMRs add 760 mm of ver
For standard 600×400mm tote transport, AMR payload class needs to be screened with a 1.2× safety multiplier on total installed load, placing typical tote duty (20–80kg) in the 50–100kg chassis band. Heavier shelf and pallet AMRs scale to 1500kg for pallet and 1900kg for material-transport platforms.
Vertical lift modules (VLMs) need at least 3.5 m of clear ceiling height, and most sit between 3.3 m and 21 m. An AMR robot entering an access bay must clear the VLM's overhead extractor, shutter, and the bay's own lintel, typically leaving only 1.5 to 2.0 m of usable working height at the picking w
AMRs (autonomous mobile robots) typically operate in aisles as narrow as 70 cm with 20 mm obstacle clearance, while traditional AGVs (automated guided vehicles) require wider guided aisles plus buffer for fixed-route turn geometry, per the Georgia Tech minimum-aisle AGV path-planning study and 2026
AS/RS storage and retrieval typically draws about 0.02 kWh per pallet cycle, with shuttle-based and crane-based systems delivering comparable per-move energy use but diverging sharply on throughput, density, and integration overhead. Below 0.05 kWh per cycle is realistic for ambient pallet AS/RS; co
AC drive motors on reach trucks outperform brushed DC drive motors in efficiency, maintenance interval, and lifecycle cost; modern Class II reach trucks have shifted to brushless AC induction drives paired with vector-controlled VFDs, while DC remains viable only for legacy fleets or full-torque-at-
350 L (≈92 gal) mini IBC tanks fill the lab-quantity gap between 200 L drums and 1000 L standard IBCs. Stainless 304 and carbon-steel versions both ship on standard 42"×48" footprints, with dimensions 47.25"–51" tall and tare weights from 215 to 475 lb depending on build.
For belt conveyors, pick 20 degree troughing idlers for stiff belts and lump feed, 35 degree as the default carrying angle for bulk tonnage, and 45 degree only when extra cross-section is worth the longer transitions and tighter skirt sealing. CEMA B4/C5 frames, transitions, and CEMA class ratings a
A load profile check gate filters unit mass, dimensions, center-of-gravity, and load-handling-device compatibility before any stacker crane is dispatched into an AS/RS aisle, cutting induction errors at the WMS/WCS handoff.
Woven polyester cord strapping delivers 650–3,000 lb break strengths with slight elongation, while extruded PET strapping bands trade that flex for higher stiffness and lower creep. Pick woven cord for shifting or rigid loads needing impact absorption, and PET band for high-tension, long-haul pallet
OSHA's Class II definition groups all narrow-aisle electric motor rider trucks with lift codes 1-3, including every order picker variant. Low-level order pickers are not Class III because the operator rides an elevating platform, which violates the Class III pedestrian/rider pallet-jack envelope.
Overhead conveyor trolleys handle a wide load range, from a few pounds on light enclosed-track systems to several thousand pounds on heavy I-beam monorails. Common per-trolley ratings: enclosed track 180-250 lb, heavy-duty enclosed track 220-440 lb, I-beam monorail 250-2,500 lb continuous, and power
A label printer is a device that outputs adhesive labels or printed markings for manual application, while a labeling machine applies labels automatically as part of a production line. The two differ in automation level, throughput, integration scope, and total cost of ownership.
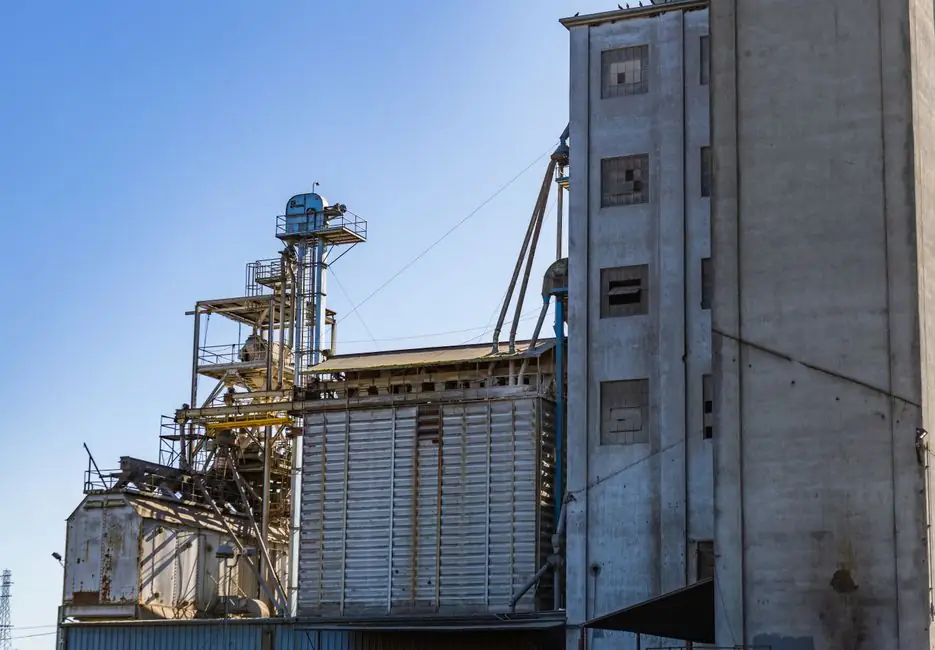
A bucket elevator is a continuous vertical conveyor using a belt or chain fitted with evenly spaced buckets, sized for high-capacity, free-flowing bulk solids. A skip hoist is an intermittent loader that hoists a single large bucket (or skip car) on rails up an inclined or vertical path, suited to b
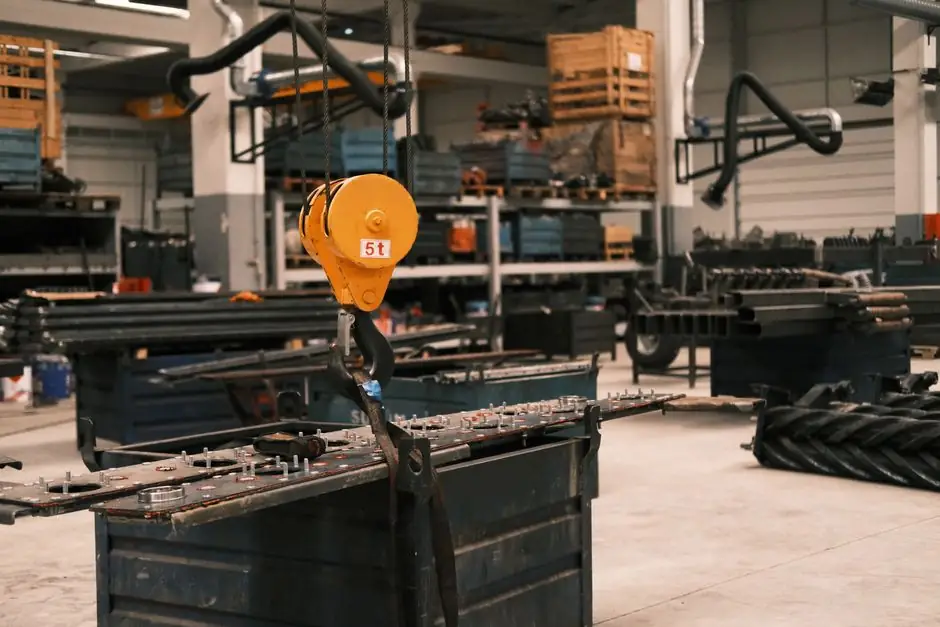
A Vertical Lift Module (VLM) is an enclosed automated storage system that stacks trays in two columns around a central extractor and delivers each tray to a single ergonomic access window, using ceiling height to reclaim up to 85–90% of the floor area that conventional shelving occupies.
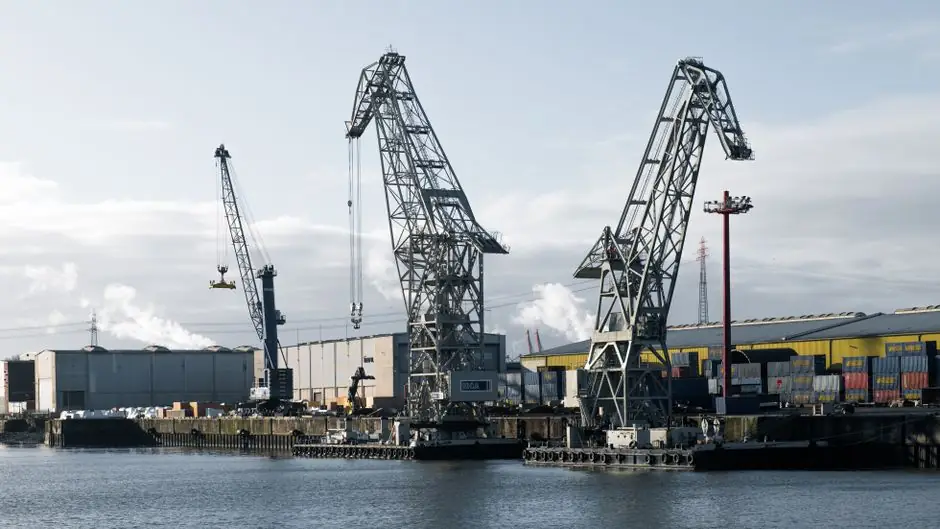
An automated stacker crane is a rail-guided AS/RS machine that runs a single aisle in a high-bay warehouse, performing coordinated horizontal travel, vertical lifting, and telescopic fork movement to store and retrieve unit loads at heights up to about 45 m, in aisles as narrow as 1.5 m, and at spee
A stacker crane is an automated aisle-bound crane that runs on floor rails to store and retrieve unit loads (pallets, bins, totes) from high-bay racking, typically reaching 30-45 m in aisles 1.5-2.0 m wide, and is the load-handling core of any ASRS in food, pharma, cold-store, e-commerce and air-car
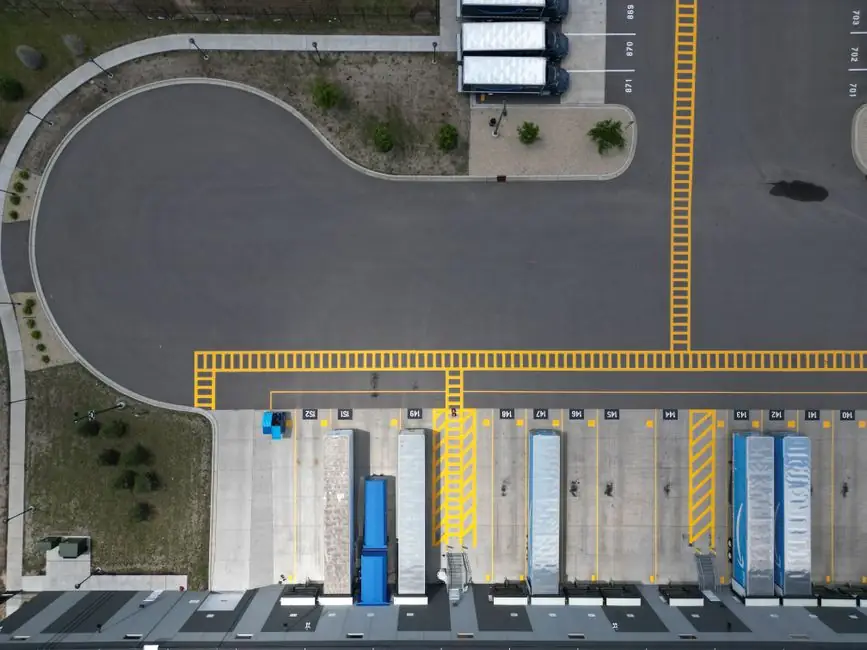
A dock leveller is a height-adjustable steel platform that bridges the gap between a warehouse floor and a truck bed, typically rated 6–15 tonnes and built from galvanised steel. Warehouses need one to keep forklifts and pallet jacks moving safely across variable trailer heights, eliminating manual
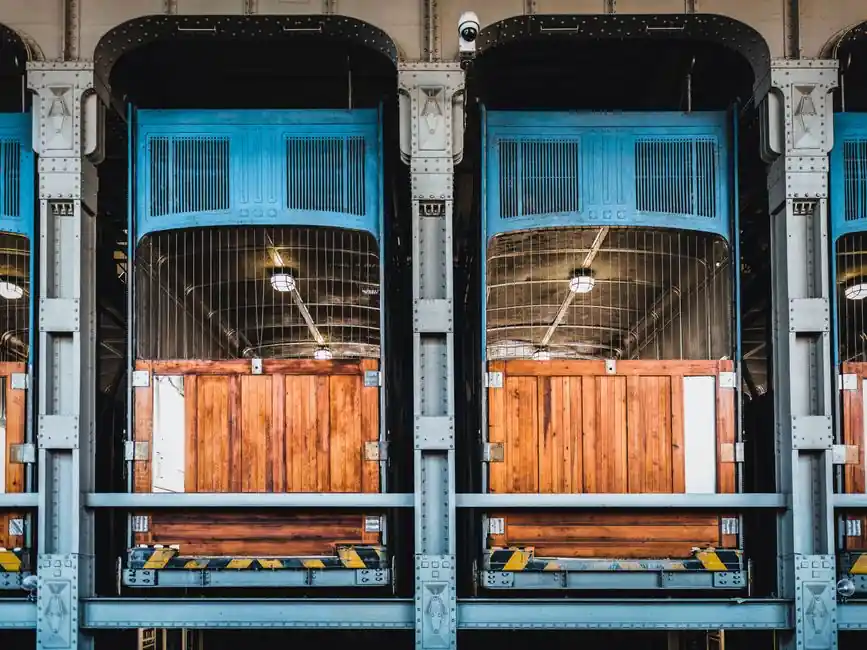
The bucket elevator boot section is the lower loading and tensioning housing where buckets scoop material from a feed inlet and where belt or chain take-up is adjusted. It matters because flooded boots, mis-leveling, and poor access drive most bucket-elevator downtime and spillage.
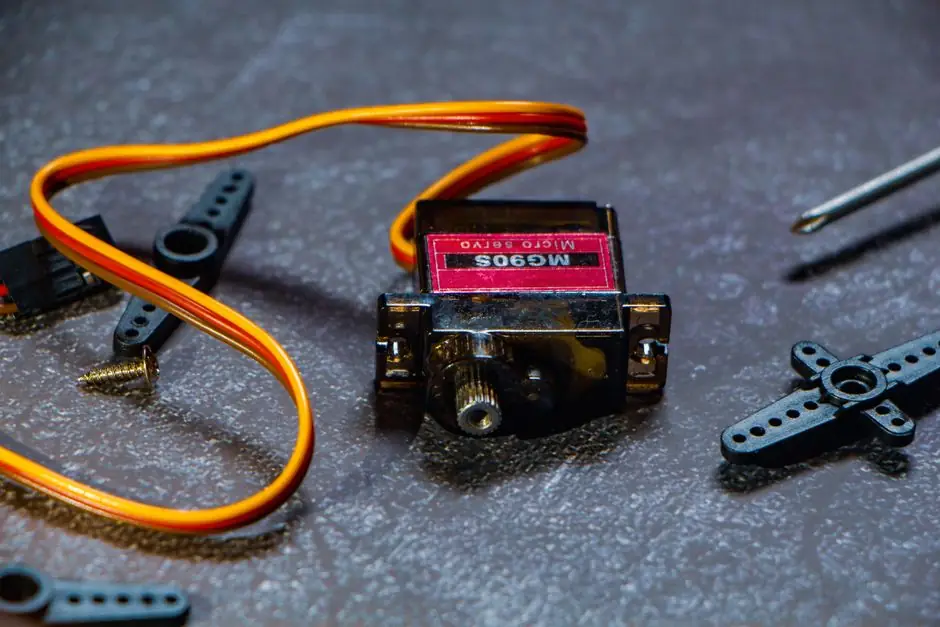
An AGV is guided along its programmed path by a navigation system combining physical path markers (magnetic tape, inductive wire, floor magnets/QR codes) with onboard sensors such as laser scanners, gyroscopes, accelerometers, and vision cameras. Path type, traffic density, and reconfigurability dec
VLM extractor vertical travel is typically adjustable up to 2.0 m/s (6.6 ft/s), with horizontal feed to the access opening around 0.7 m/s (2.3 ft/s). End-to-end tray retrieval commonly lands in the 8–15 second range once SKU slotting is tuned.
An 8 ft recessed dock leveler set 12 in. below dock face creates roughly a 12.5% downward grade, which exceeds the 7% limit of a manual pallet jack but stays inside the 15% cap for an internal combustion forklift.
Label registration accuracy on a labeling machine is the positional repeatability of each label relative to a reference, typically expressed as a ± mm tolerance on the container. Servo-driven systems commonly hold ±0.5 mm; stepper-driven entry units drift to roughly 1.5 mm, and the gap is set by enc
EP630/4 is a DIN 22102-style conveyor-belt designation meaning a polyester/nylon (EP) fabric carcass with a minimum breaking strength of 630 kN/m and 4 plies. The standard format is DIN 22102 1000 EP 630/4 6/2 Y, where 1000 is belt width in mm, 6/2 is top/bottom cover thickness in mm, and Y is the D
Walkway clearance under overhead conveyors is 8 ft minimum for foot traffic and 10 ft or more for forklifts, measured from the lowest-hanging component. U.S. mining rules cite a 7 ft baseline with warning signs as a fallback.
Strapping bands secure, bundle, and palletize loads for shipping and storage using flat loops in four materials: PP, PET, steel, and woven composite. Selection hinges on load weight, tensile strength, elongation recovery, and transit distance, with PET covering most industrial applications.
Vertical lift modules (VLMs) configured with access openings on two separate floors use a single lift column spanning the levels, with up to 3 bays at the front, rear, or stacked floors, and payload capacities up to 2,200 lbs per tray. Specifiers should confirm floor-loading, multi-bay interlocks, a
A three-unit VLM pod, one operator, software-linked, runs as a baseline for high-throughput picking because the operator picks from one unit while the other two concurrently retrieve the next trays, eliminating idle time and matching parallel-machine logic described in peer-reviewed throughput model
VLM manufacturers typically ship units in 4 to 6 sections per module, with on-site assembly plus commissioning commonly running 2 to 5 working days per unit depending on height and floor prep.
Vertical Lift Modules (VLMs) store trays in 25 mm vertical increments and re-measure every load with an onboard height scanner, recovering up to 85% of floor space versus conventional shelving.
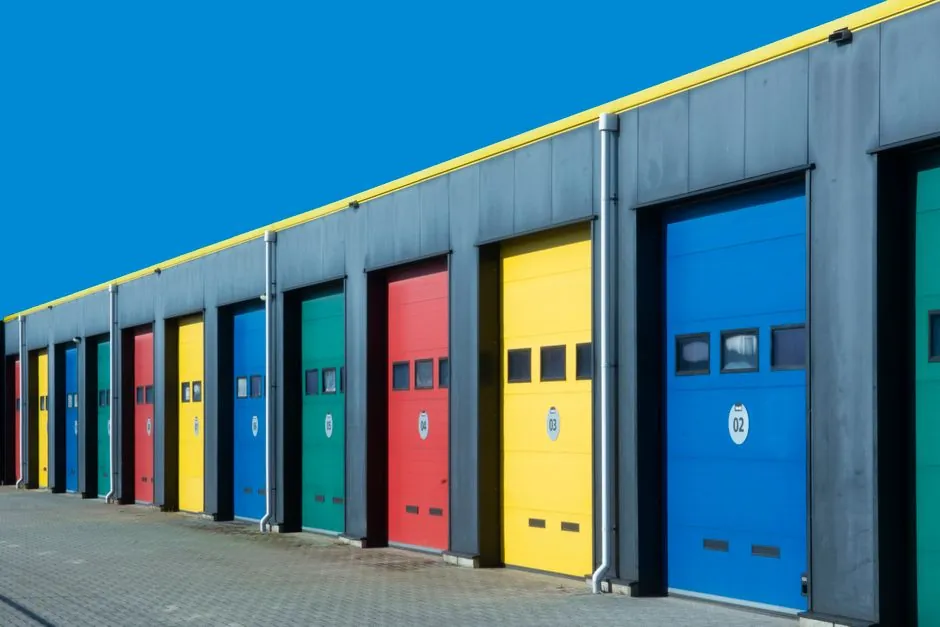
Vertical storing dock levelers let an overhead door close directly against the pit floor, eliminating the perimeter gaps that a pit-style leveler leaves around a door; in cold storage this is the single biggest lever for cutting air infiltration, frost, and compressor load. Pit-style levelers still
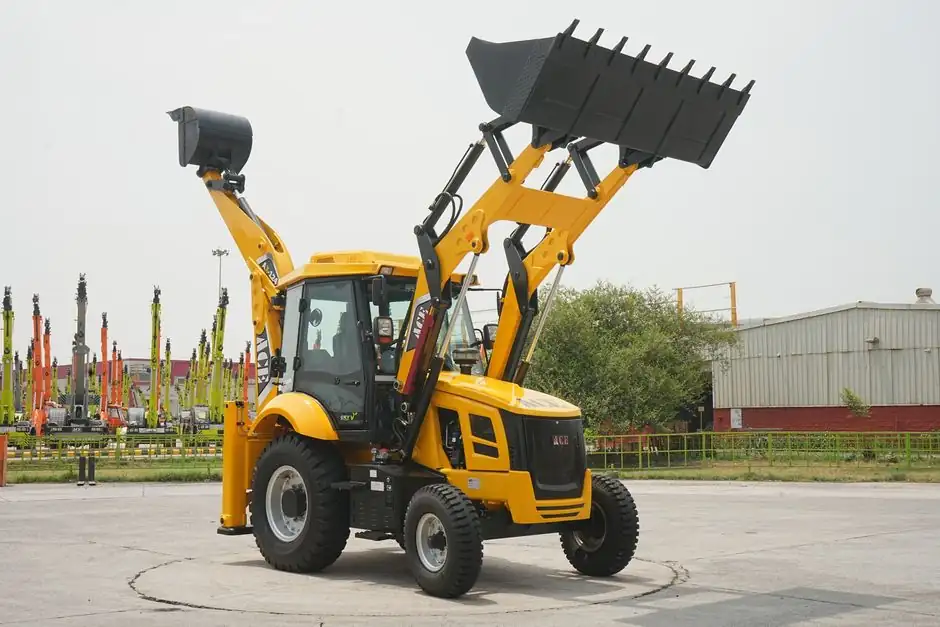
Vertical lift modules (VLMs) beat vertical carousels for tall facilities, heavy payloads up to 2,200 lb per tray, and variable-SKU inventory, with 85% footprint reduction and dual-tray pre-staging. Vertical carousels win for low ceilings under 20 ft, uniform small parts, and simpler maintenance, wit
Vertical lift modules outperform vertical carousels for variable-SKU, high-ceiling goods-to-person picking: VLM trays scale to 52 ft tower height and 2,200 lb payloads, while carousels cap near 32 ft and 1,430 lb per carrier. Choose VLM for mixed inventory; choose a horizontal carousel pod or vertic
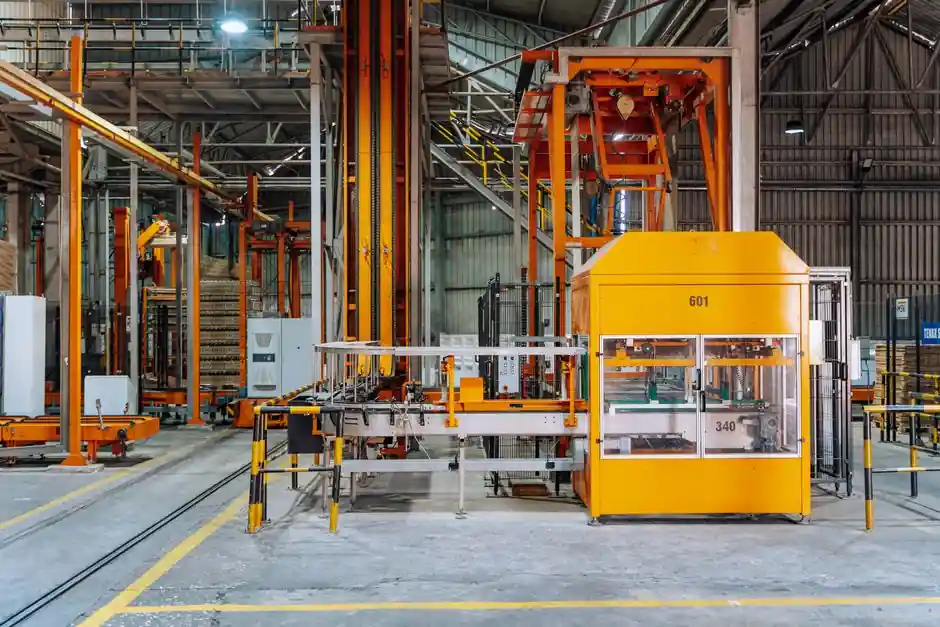
Vertical lift module tray delivery positions the picking opening between belt height and shoulder height, the "golden zone," eliminating ladder climbing and overhead reaching in goods-to-person order picking. Specifying tray height optimization requires anchoring pick windows to anthropometric data,
VLM tray dimensions are not a single industry standard: common widths are 96 to 144 inches with a total range near 3 to 21 feet, depths sit between 30 and 48 inches, and unit heights scale from about 7.8 feet to 68.9 feet depending on the OEM model family.
Vertical lift module throughput is rated 100-300+ lines or trays per hour, with single-elevator units at the low end and dual-elevator or podded configurations reaching 300+ LPH depending on tray travel, operator skill, and zoning. For order picking above 200 LPH, pair two or more VLMs in parallel r
Vertical lift modules reach up to 99.9% inventory accuracy versus manual shelving, which typically trends lower as SKU counts grow; VLMs also reclaim up to 85% of floor space and cut picking time by up to 66%.
Vertical lift module installation is governed by three hard building constraints: clear ceiling height (typically 14 ft 7 in to 68 ft 11 in), distributed floor load from a fully loaded unit, and service envelope around the access bay. Specs that miss any of these three force a redesign, a slab pour,
Vertical lift modules (VLMs) for pallets versus for small-parts trays differ in tray geometry, load rating, ceiling requirement, and throughput profile. Pallet VLMs typically need 30+ ft clear height, while small-parts VLMs operate effectively in 20-25 ft ceilings and reclaim 600-1,000+ sq ft per un
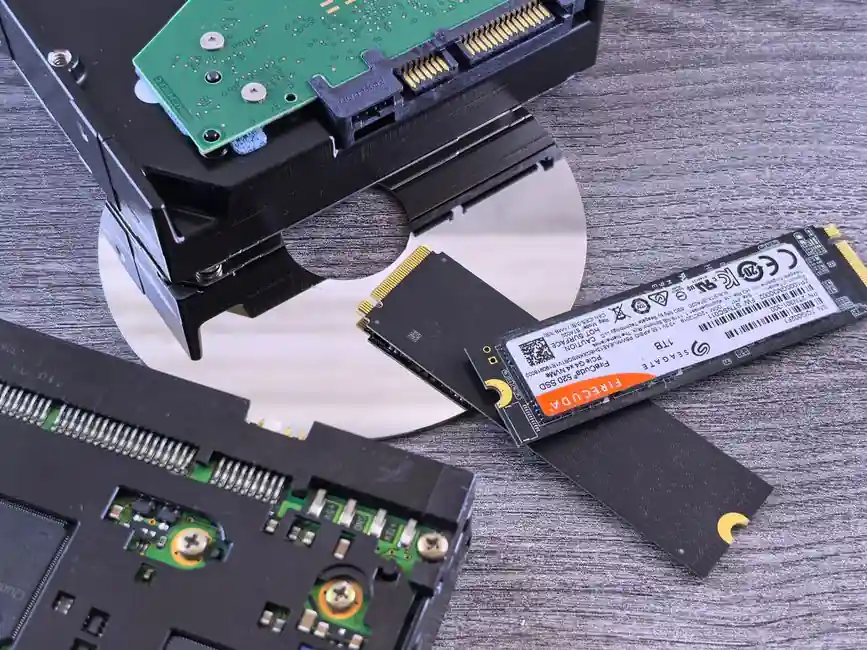
Vertical Lift Modules (VLMs) reduce small-parts storage floor area by 60–90% versus static shelving, with OEM data showing 75% floor recovery common and up to 1,000 sq ft reclaimed at 40 ft ceilings. Trade-offs are higher unit cost, depth requirements of 10–18 m, and throughput capped at 50–180 tray
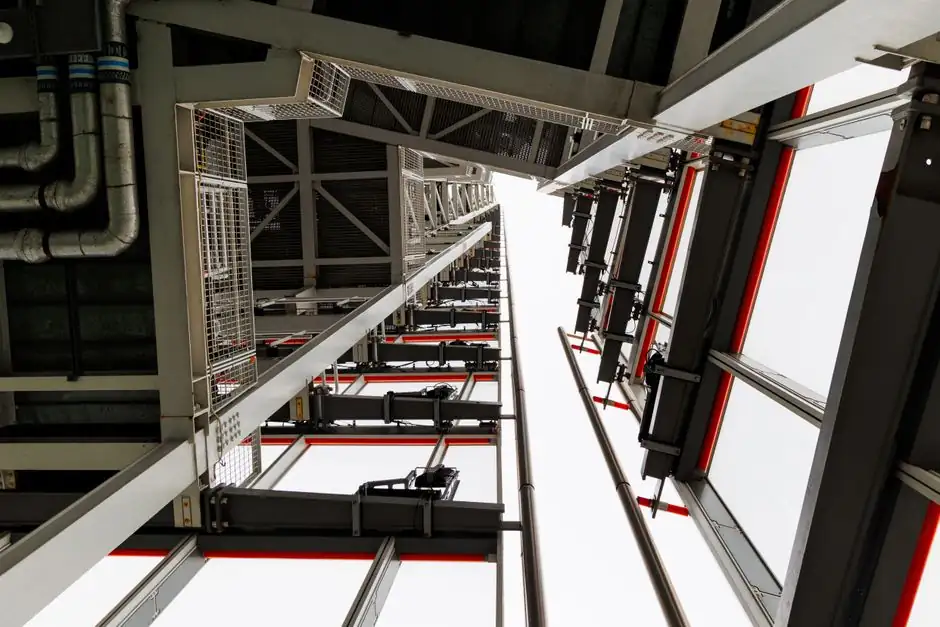
Dynamic slotting inside a Vertical Lift Module (VLM) lets the controller re-measure tray clearances via an onboard height sensor on every putaway, so fast-moving SKUs automatically migrate to the access opening. Combined with ABC analysis and pick-to-light guidance, this collapses travel time and cu
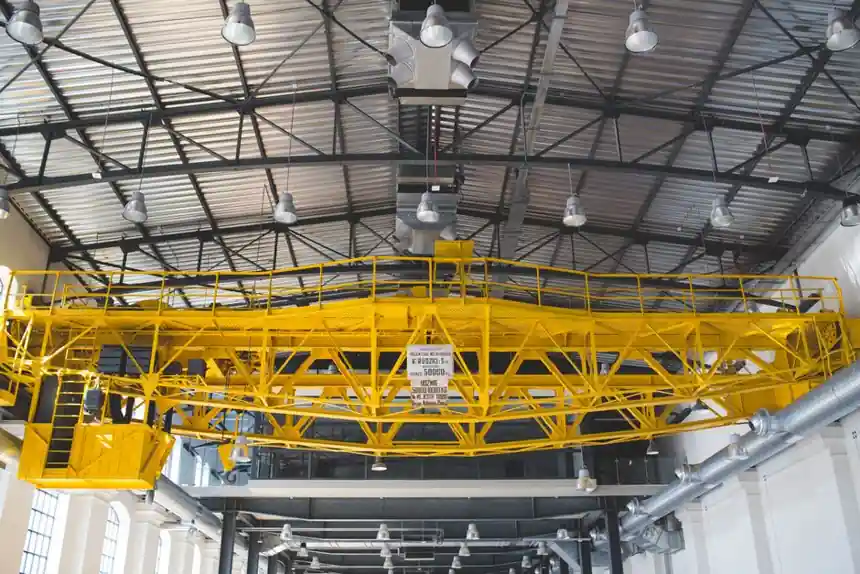
Vertical lift modules (VLMs) scale roughly 8 to 78 feet in 4-inch height increments, fitting ceilings from 16 to 35+ feet; below 30 feet clear height favors VLMs, while unit-load ASRS typically needs 30+ feet.
Vented elevator buckets with 1/8 in (3.175 mm) holes raise fine-powder bucket fill by releasing trapped air, preventing vacuum-induced carryover. Aggressive Vent #3 or #4 patterns suit dense powders like cement, while high-density commodities and high-speed centrifugal legs both benefit.
VDI 2198 defines Ast (Aisle stacking width) as the minimum rack-to-rack clearance a truck needs to deposit a pallet at 90 degrees, computed as Ast = Wa + load length + safety margin a. For reach trucks, the standard uses the geometric form Ast = Wa + sqrt((l6 - x)^2 + (b12/2)^2) + a, where l6 is loa
VDA 5050 is a vendor-neutral MQTT/JSON interface, jointly maintained by VDA and VDMA, that lets AGVs and AMRs from different manufacturers run under one master fleet controller. Version 2.x adds actions, state, and factsheets on top of the original order/topic layer, with 1.x released 2019 and 2.0 p
ANSI/CAN/UL 3100:2021 is the first-edition binational Standard for Safety for Automated Mobile Platforms (AMPs), covering battery-operated mobile platforms used for lifting, carrying, picking, and towing in commercial and industrial settings. It is the U.S./Canada reference spec integrators
Three AGV classes dominate factory and warehouse spec sheets: forklift AGVs, tugger/tow tractors, and unit load AGVs. Each fits a different load profile, payload mass, and aisle geometry, and mixing them up is the most common specification error in greenfield intralogistics projects.
AGV selection is driven by load handling method: tow tractors, unit load carriers, forklift, heavy-payload direct-load, cart, and lift/rotate AGVs cover capacities from under 1,000 lb to 15,000 lb. Match vehicle class to payload weight, lift height, aisle width, and indoor/outdoor duty cycle before
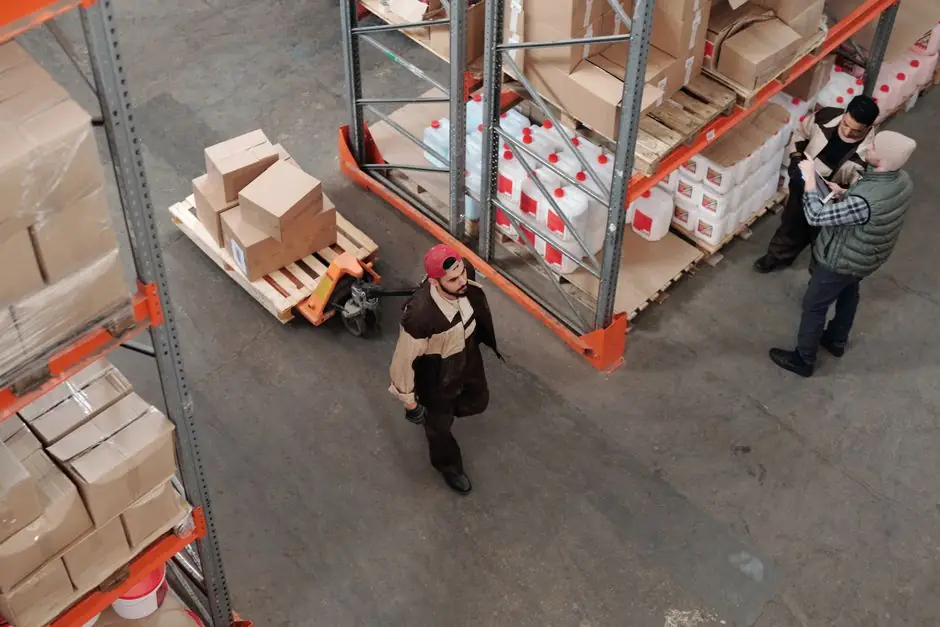
Tugger, unit-load, and forklift AGVs split cleanly by payload interface: tuggers pull trains of carts, unit-loads ride on a deck or conveyor, forklifts lift and rack. Verified 2026 hardware pricing spans $15,000 for entry AGCs to $200,000+ for VNA-class forklift AGVs, with the type chosen around rac
Type A, B, and C FIBC bulk bags are three of the four IEC 61340-4-4 electrostatic classifications for woven polypropylene bulk containers, differing in static control, grounding requirements, and permitted hazardous-area use. Type A offers no static protection, Type B limits discharge energy via low
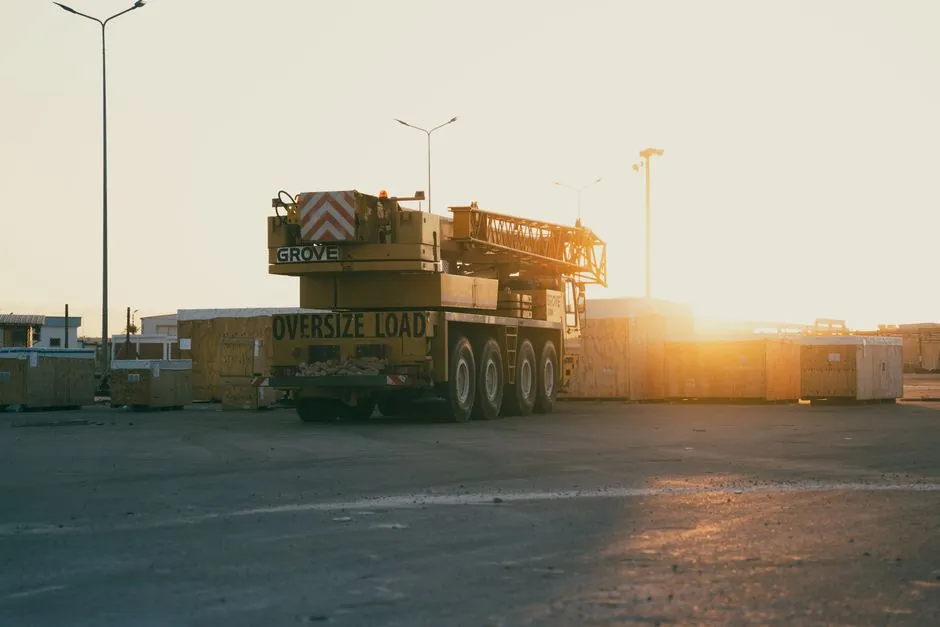
For wide-load or oversize truck operations, 3.4 m (≈11 ft) wide weighbridges give roughly 2.5 ft of lateral clearance vs. ~1.5 ft on a 3.0 m deck, the practical reason most US sites handling over-8.5 ft vehicles pick the wider platform. A 3.0 m scale is acceptable for standard highway trucks on stra
An 80,000 lb gross vehicle weight (GVW) on a five-axle tractor-trailer is the U.S. federal Interstate cap, paired with 20,000 lb single-axle and 34,000 lb tandem-axle limits, and any truck scale used to verify this class 8 combination must be sized for 80,000 lb minimum legal load with margin.
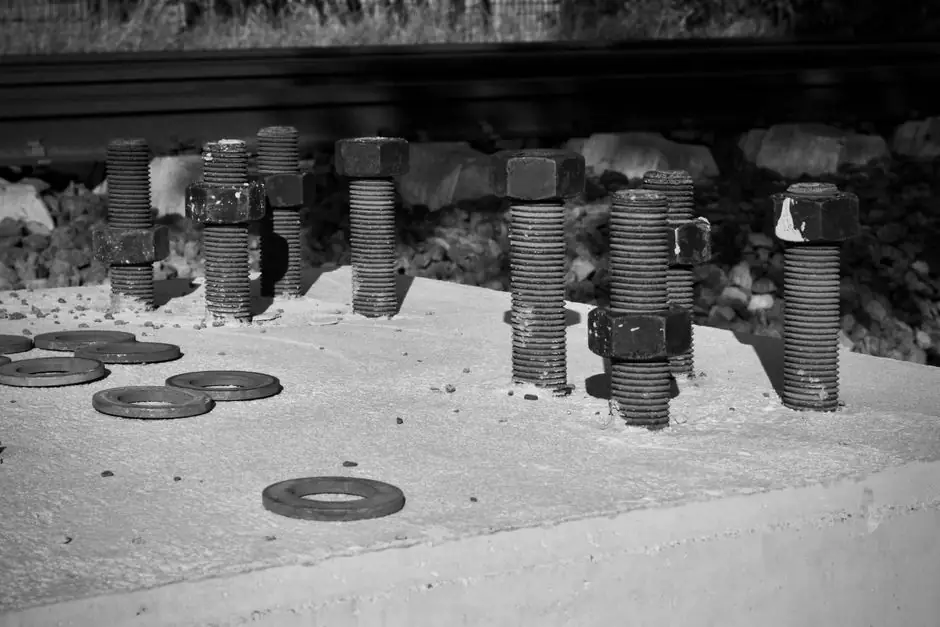
Truck scale foundation rebar and anchor embed plates form a cast-in-place steel-to-concrete load path that beats post-installed wedge anchors on shear and tension capacity. Spec writers call for 3/4 in. diameter anchor bolts on pier-only layouts and 5 in. embed plates with four 1/2 in. studs as the
Truck scale deck corrosion from chloride deicers is best controlled by hot-dip galvanizing the steel frame to roughly 70-year maintenance-free life, with industrial polymer mortar topcoats specified where chemical or acid attack accelerates steel loss beyond road-salt exposure alone.
Troughed belt conveyors carry roughly 30% more material at 35° than at 20° trough, and roughly twice the volume of a flat belt of the same width, making them the default for bulk solids above ~1,000 TPH. Flat belts remain the right pick only for short feeder runs, high angle-of-repose materials, and
Climate-controlled Vertical Lift Modules (VLMs) deliver factory-equipped temperature and humidity setpoints between roughly 15 and 25 °C with 30 to 60 % RH for sensitive parts storage. Modula, Kardex, and Material Handling & Storage offer integrated cleanroom, ESD, and dry-room variants for aerospac
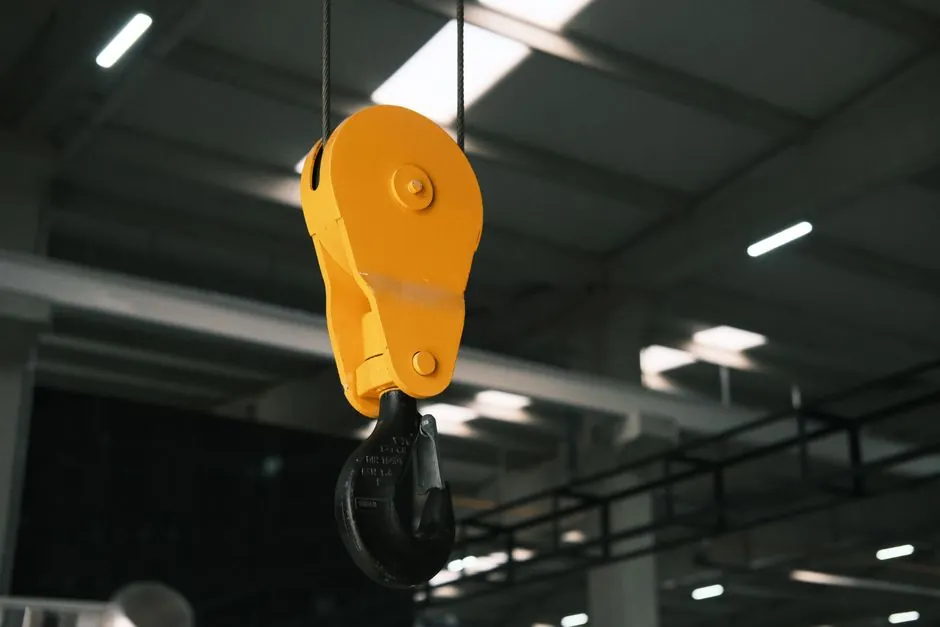
Telescopic fork stacker crane OEM extension stroke typically ranges 600–2200 mm, paired with 1000–1500 kg load capacity and –25°C to +70°C operating envelope for ASRS aisles.
Teardrop pallet rack beam capacity ratings are published as uniformly distributed load (UDL) per pair, ranging from about 2,100 lbs (8 ft slim profile) to 6,480 lbs (4 ft heavy profile) per manufacturer, with ratings governed by RMI deflection limits of L/180.
Swing gates and drop gates are the two dominant conveyor crossover choices in distribution centers; swing gates win on low cost and one-person operation, while drop gates win on traffic frequency and full-pallet lift-truck passage. For most plant engineers, the decision is a frequency-vs-footprint t
Stretch sleeve labelers apply labels mechanically with no heat, suiting large PET jugs and cold-fill lines; shrink sleeve labelers use heat or steam tunnels to conform film to bottle contours, dominating full-body 360-degree graphics and tamper-evident neck bands. Pick stretch for energy and recycla
Strapping band type A (unembossed) holds higher absolute tension but loses retained tension under load drop, while type Z (embossed) grips the seal better and keeps more residual tension on settling loads; pick A for rigid heavy pallets, Z for compressible or stacking-sensitive goods. The decisive v
Strap size for a pallet load is set by the break-strength formula (Pallet Weight × 1.5) ÷ Number of Straps, then matched to material and width: PP at 12–19 mm covers 120–600 lb ranges, PET 1/2" hand-grade reaches 750 lb, and steel is reserved for hot or sharp-edged loads. Static palletized loads use
PET strapping yields roughly half the meters per kilogram of PP strapping at the same width, with a verified 19 × 1.0 mm PET grade at ~10.7 m/kg versus 9 × 0.6 mm PP at ~33.8 m/kg. Choose PP for light indoor loads under ~270 kg break force, and PET for heavy pallets above 300 lb where tension r
Strapping band break strength scales with both width and thickness, not width alone: a 1/2" x .020" high-tensile steel strap rates 1,430 lb, while a 3/4" x .031" of the same grade reaches 3,250 lb. Polyester and polypropylene overlap at the low end (300-1,800 lb) but never match steel above ~3,500 l
Industrial strapping divides into four working families (steel, polyester, polypropylene, woven/composite), each selected by load weight, edge sharpness, elongation need, and corrosion exposure. Steel remains the only option for very heavy, hot, or sharp-edged loads; polyester and cord composite dom
Stepped pipeline design in pneumatic conveying increases pipe diameter downstream to offset air expansion, keeping velocity near 4,000–8,000 fpm. Best applied on long, high pressure-drop (≥7 psi) dilute-phase lines; verify downstream velocity stays above saltation and choke limits.
For light-duty enclosed track overhead conveyors under 3,000 lb, pick steel for high-cycle, abrasive, or heat-exposed duty and pick aluminum for clean rooms, anodized wash-down, or where reduced dead-weight enables longer spans.
Cold-rolled steel strapping is stocked from 12.7 mm to 31.75 mm width and 0.38–1.27 mm thickness, with break strength scaling from roughly 3,600 N (9.5 mm) to 17,881 N (31.75 mm) per Signode, FROMM and AAR-certified mill data.
Steel strapping has the highest break strength and lowest elongation; polyester (PET) has higher tensile strength and elastic recovery, suiting loads that settle; polypropylene is the lowest-cost plastic, suited to light-duty unitizing. Choose steel for sharp-edged heavy loads, PET for heavy loads t
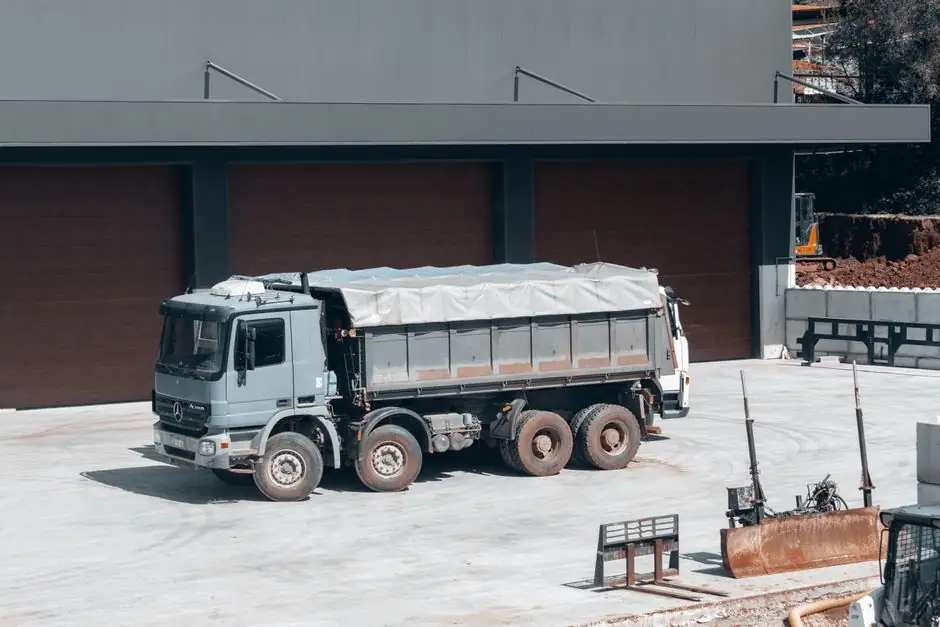
Steel deck truck scales install in roughly one day while concrete deck scales need up to 30 days of cure time, and concrete weighs about four times more, so the choice depends on timeline, relocation plans, weather exposure, and total ownership cost. Use steel for fast install, lower upfront cost, o
Standard-pitch screw conveyors use flight pitch equal to diameter for horizontal service to about 10 degrees; short pitch (2/3 D) and half pitch (1/2 D) are specified for inclined, vertical, and fluidizing material duty, while cut flights add mixing. Selection is governed by angle, material fluidity
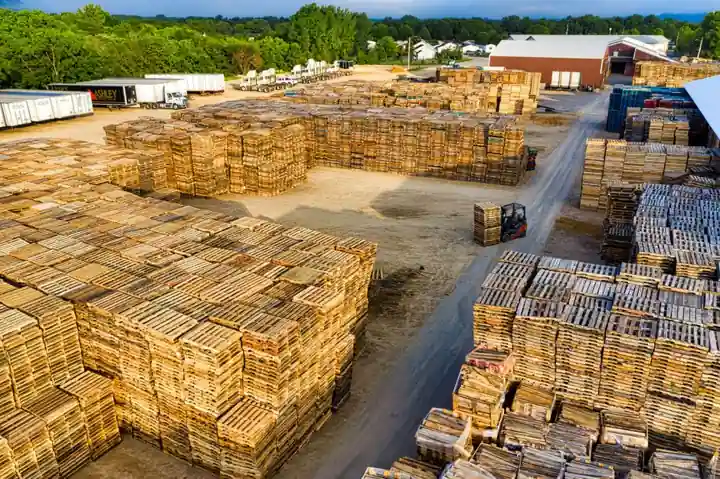
Standard AGV load capacity for unit-load pallet transport spans 1,000-1,500 kg for common pallet-truck models and scales to 30,000 kg (66,000 lb) on engineered deck platforms, with selection driven by pallet interface, lift height, and fleet coordination rather than a single rated tonnage[S
Stainless steel strapping band (Types 201/304/316) offers 1,500 lb break strength and superior corrosion resistance; aluminum strapping band is roughly one-third the weight, easier to form by hand, and specified where non-sparking, non-magnetic, or weight-sensitive installation matters. Pick stainle
For pole-mount banding, Type 304 stainless steel is the default choice for most utility and sign-mounting jobs, while Type 316 is specified where chloride exposure (coastal, de-icing salt, refinery) is a factor, and Type 201 is reserved for budget-driven light-duty interior or dry-region use. Bandin
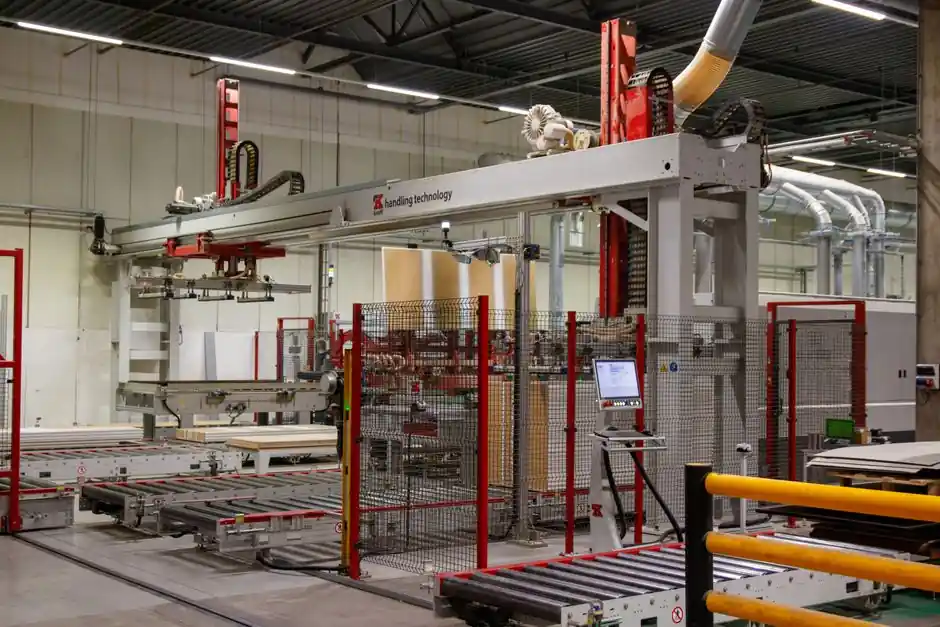
Single-deep stacker cranes give 100% direct pallet access; double-deep stacker cranes trade that for roughly 1.5–2× storage density by storing two pallets per position using a telescopic fork. Pick single-deep for high SKU variety, FIFO, and fast retrieval; pick double-deep for medium-turnover bulk
Stacker-crane side loaders (cantilever-arm or trilateral fork units) can store long bars, profiles, pipes and plates up to roughly 6.2 m in single-aisle AS/RS racks, replacing floor-level cantilever with high-bay density. They suit makers needing 6-12 m length handling with no forklift traffic, not
Stacker crane aisle width and rail tolerance are engineered requirements, not construction finishes: aisle clearances typically add 100-200 mm over the load envelope, while floor rail levelness is held to roughly ±2-3 mm over 2 m, per FEM 9.832 and CMAA/AISC runway practice.
Stacker crane rail tolerance is an engineered parameter, not a finish spec: bottom-rail and upper guide-rail alignment, rack upright straightness, and floor flatness must be coordinated to millimeter-level accuracy, with AS/RS systems running up to 45 m high and 1.65 t unit loads.
Stacker crane price is driven primarily by four hardware-bound variables: lift height (up to 148 ft per Interlake Mecalux MT-5), horizontal travel speed (up to 6 m/s on Jungheinrich miniload, 2.5 m/s on Lödige), payload (1.1–1.65 t class on single-mast, 1,300 kg on air-cargo units), and the load han
Steel stacker crane masts handle heavier unit loads and taller installations (up to 148 ft, 1.65 t per pallet), while aluminum masts cut mast weight by 50 to 70 percent and resist corrosion in cold or coastal warehouses. The material choice hinges on lift height, payload, and whether the crane is fi
Single-command stacker crane cycles move one load per trip, while dual-command cycles combine a storage and a retrieval in one run, cutting round-trip time by roughly 30% (Meneghetti, 2011) and requiring matched storage/retrieval demand. Use dual-command where inbound and outbound queues overlap con
Single-mast stacker cranes suit light to medium unit loads (1.1-1.65 t) and compact aisles, while double-mast designs handle heavier payloads and reach higher bay elevations. Choose single-mast for sub-1.65 t loads under 148 ft; pick double-mast for 5,000 kg-class loads, 42 m reach, and reduced sway
Split housing screw conveyors add hinged or bolted flanged clamshell access to the standard tubular casing, cutting internal cleanout time and supporting food-grade washdown, while solid tube housings win on sealing, pressure containment, and inclined conveying over 15 degrees per KWS design guidanc
Single-mast and twin-mast vertical lift modules split on three hard constraints: working height, payload, and aisle width. Twin-mast dominates above 12 m and 250 kg; single-mast wins below 150 kg in sub-1 m aisles. Extractor count is a separate VLM decision, independent of mast count.
For inclines below ~40°, chevron (V/Y) cleated belts are the lower-cost, simpler choice; for 45° to vertical lifts, corrugated sidewall belts with T-cleats are mandatory. Both options run on a belt conveyor frame, but the sidewall design adds corrugated sidewalls (60–400 mm) and cross cleats (40–360
Internal or external VLM access bay is not a marketing preference, it is a layout decision driven by throughput, ceiling height, and aisle width. Internal bays fit tight footprints, external bays support dual delivery and ergonomic crane-assist picks; dual-extractor units can exceed 100 trays/hour.
A pit dock leveler is almost always welded into the formed pit, not only bolted: the rear hinge angle gets a continuous structural weld, the shims are welded to the frame, and on lower-capacity units 6-inch stitch welds are acceptable. Bolted edge-of-dock units exist, but they are a different produc
Shaftless screw conveyors are specified over shafted units for sludge and other sticky, fibrous, wet biosolids, trading a UHMW liner wear part for a higher 35–45% fill rate and elimination of hanger-bearing obstructions. Shafted designs still win on long horizontal runs above 3 m, higher allowable R
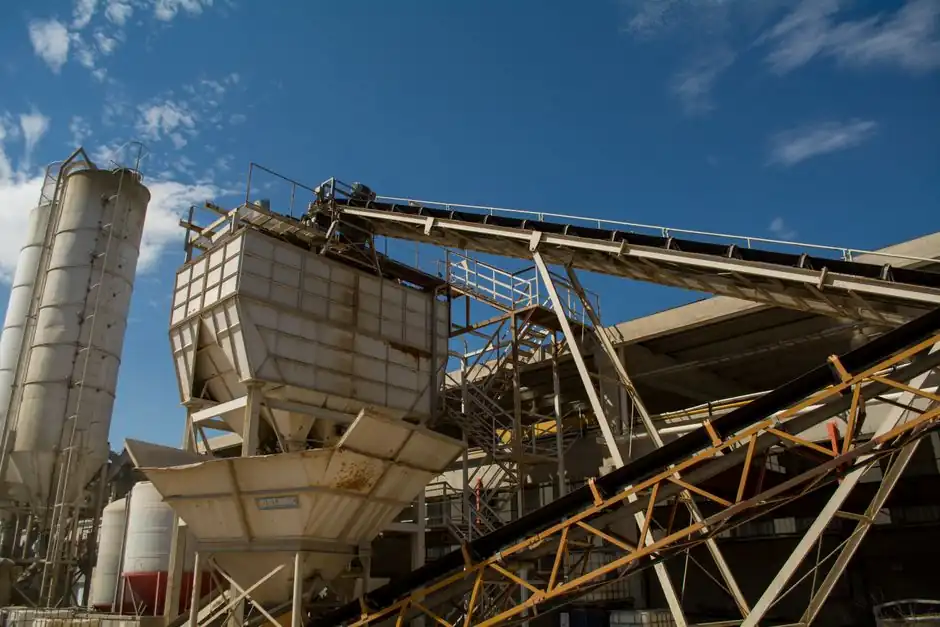
For screw conveyors, shaft-mounted reducers mount directly on the screw drive shaft and eliminate the low-speed coupling and base, while end-mounted (adapter/flange) drives bolt to the trough end and dominate the market due to lower installed cost.
Semi-automatic tabletop round bottle labelers typically deliver 20 to 60 bottles per minute, equivalent to roughly 1,200 to 3,600 bottles per hour, making them the default for short production runs and low-volume packaging lines.
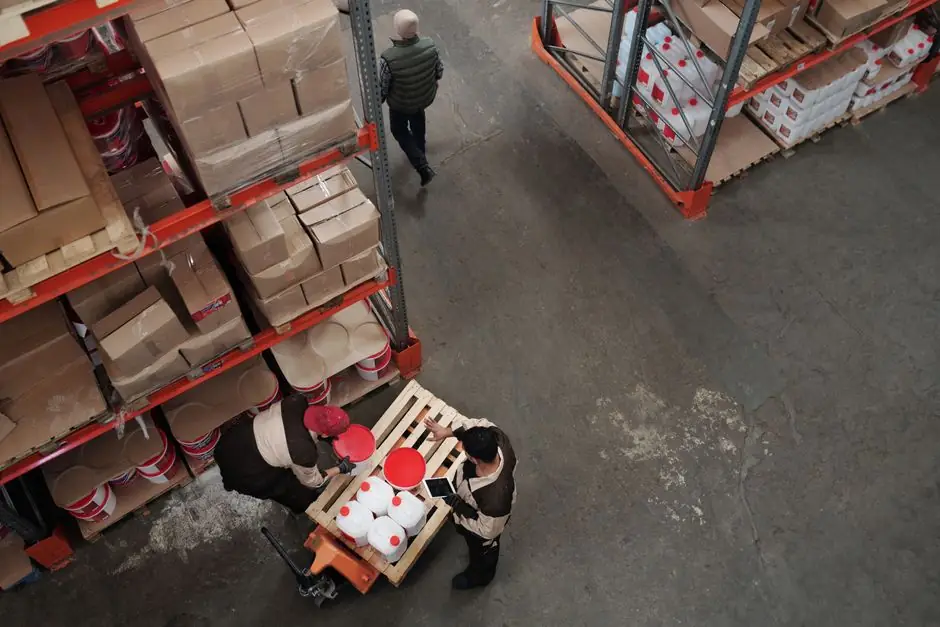
Selective pallet rack and drive-in pallet rack are the two workhorses of warehouse storage, but they solve opposite problems: selective gives 100% pallet access at lower density, while drive-in delivers the highest density by sacrificing access and running a LIFO (last-in, first-out) rotation. Pick
Seismic design of stacker-crane masts and floor-rail anchoring is governed by the same two-rail single/twin-mast geometry used in AS/RS service, with rail reactions, anchor embedment, and mast base clearance sized for site seismic intensity. Bottom-rail, top-rail, and anchorage details vary with cra
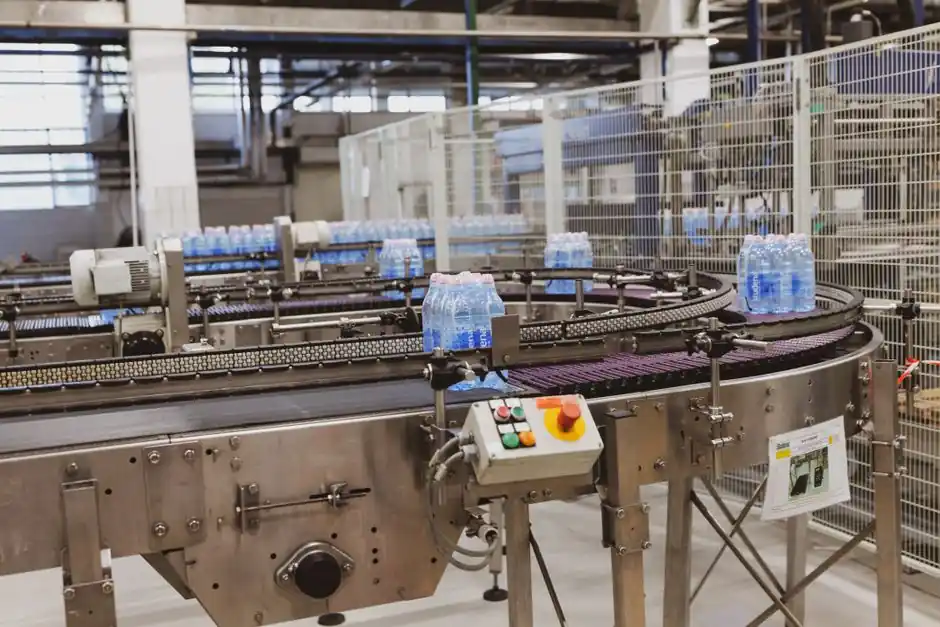
Sectional flighting carries uniform thickness from inner to outer edge and is the go-to choice for abrasive or heavy industrial service, while helicoid flighting is cold-rolled as a continuous helix, costs less, and suits lighter or fine/sticky materials. Sectional flighting is available in heavier
10 gauge mild steel measures 0.1406 in (3.572 mm) under the U.S. standard gauge, while 3/16 in plate is 0.1875 in (4.763 mm), a 0.0469 in (33.4%) thickness jump. Pick 10 Ga for light/medium abrasive duty under 24 in troughs; choose 3/16 in plate for heavy abrasive, long-span, or 24 in+ service.
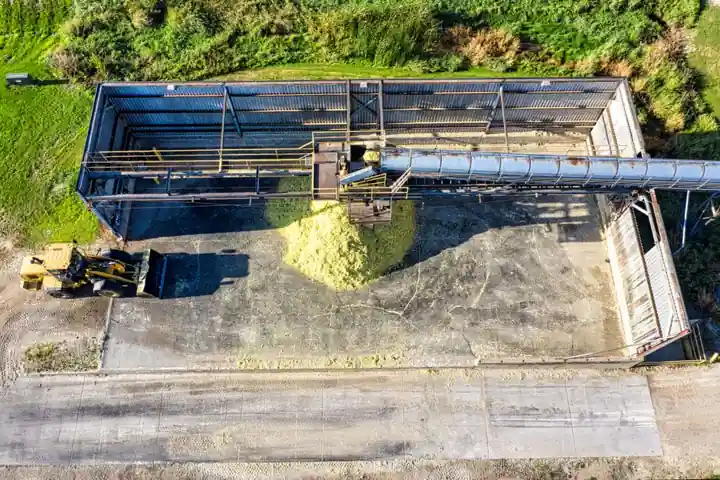
Screw conveyors are typically designed to operate at 15%, 30%, or 45% trough loading. 45% is the practical ceiling for light, free-flowing, non-abrasive bulk materials, while 15% is reserved for dense, sluggish, or highly abrasive solids.
Abrasive bulk solids cut screw-conveyor service life by attacking flight faces, trough walls, and hanger bearings; specify flight and trough material from abrasion-resistant steel (AR400/450, Hardox 400-500) or 316 stainless for corrosive-abrasive service, with trough loading held at the lower end o
For screw conveyors handling mildly abrasive dry bulk, A36 carbon steel (~100 BHN) is the default; switch to AR400 (~400 BHN, 4x the wear life) for sand, mineral, or metal-recycling service, and to stainless steel only when corrosion, washdown, or food-grade exposure overrides abrasion cost. Stainle
CEMA standard flight-to-trough clearance is 1/2 in radial, while 1/4 in clearance is a tight, application-specific option that costs more and risks rub. The choice is governed by screw OD tolerance, trough ID tolerance, CEMA screw deflection, and material fines behaviour.
Screw conveyor flight pitch-to-diameter ratio (P/D) governs capacity, incline behaviour, and material agitation. Standard pitch equals screw diameter, short pitch is 2/3 D, half pitch is 1/2 D, long pitch is 1.5x D, with selection driven by incline angle, material flowability, and feeder versus conv
Screw conveyor hanger bearing spacing is set by the screw length between couplings: standard practice keeps each hanger at 8 to 12 feet (2.4 to 3.7 m) of screw span, matching CEMA grouping tables for shafted conveyors up to 3 7/16 in. shafts.
For sectional screw conveyors, designers must choose between a solid coupling-shaft assembly (inserted and bolted into the screw center pipe) and a pipe-shaft (flanged shaft-to-pipe) design. The coupling-shaft route is the CEMA stock default, while the flanged pipe-shaft design trades field servicea
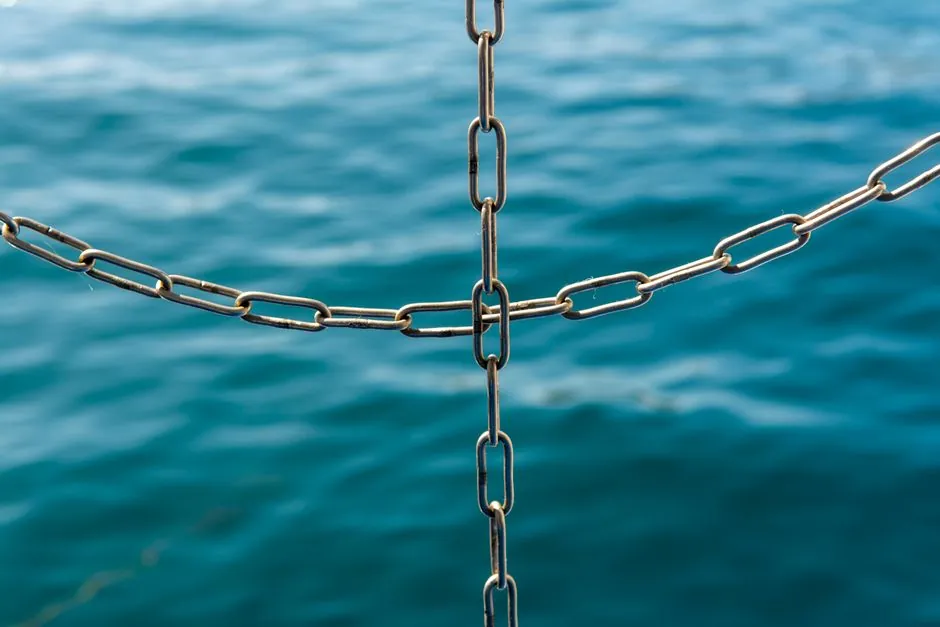
Round link, bush (pin-bush) and plate-link chains are the three traction options for vertical bucket elevators; round link suits hot or abrasive bulk materials, pin-bush central chain suits high-capacity NE-type elevators, and plate-link (with optional rollers) handles the heaviest cement and fertil
Spring-assisted roller conveyor lift gates cut operator lift force to roughly 20 lb, while gas-strut and counterweight alternatives trade maintenance, self-powering and slam-latch behaviour for ergonomic gain. Pick by cycle count, gate weight and the level of maintenance access your floor team can a
Roll-fed hot-melt OPP wrap labelers win on cost-per-label and throughput above ~10,000 containers/shift, while pressure-sensitive wrap labelers win on changeover speed, SKU flexibility, and clean operation. Pick roll-fed for long beverage/food runs on cylindrical containers; pick pressure-sensitive
Standard reach trucks need roughly 2,600-2,900 mm of clear stacking aisle for Euro 800x1200 mm pallets, calculated as turning radius plus load distance plus pallet depth plus 200 mm safety clearance. Counterbalance electric forklifts need 3,400-3,900 mm for the same load, so a facility that does not
For ISO pallets of 1000 x 1200 mm, a reach truck needs roughly 2.6-2.8 m of working aisle when the load is taken crosswise (forks engaging the 1000 mm side) and roughly 2.7-2.9 m when taken lengthwise; crosswise is usually the tighter option, and the absolute practical floor for single-depth reach o
Rail-mounted stacker cranes (AS/RS) run on a fixed floor rail plus an upper guide rail and serve aisles 1.5 m wide up to 45 m tall; aisle stackers are mobile forklifts that need wider floor space and lower reach. Choose rail-mounted when storage density and 24/7 throughput drive ROI, aisle stacker w
Pick PVC for light, clean, packaged-goods unit handling at roughly 30%–50% lower belt weight, and pick rubber when loads are heavy, abrasive, or sub-zero, with rubber reaching 660+ PIW tensile strength and PVC topping out near 250 PIW. The decision hinges on duty class, temperature, and chemical exp
Pallet flow rack is a FIFO gravity system reaching 12+ pallets deep with brakes for speed control, while push-back rack is a LIFO cart system limited to 2-6 pallets deep per lane, with the right pick depending on rotation, depth, and SKU profile.
Print-and-apply labelers generate variable data and apply labels in a single inline step; pre-printed label applicators dispense pre-made labels at higher speed with lower per-unit print cost. Choice depends on SKU variability, run length, line speed, and label-data changeover frequency.
Pressure-sensitive labelers and shrink-sleeve labelers serve the same packaging line but diverge sharply on container shape, throughput, and unit cost: PSL is best for flat to moderately curved surfaces and short to mid runs, while shrink sleeves deliver full 360° coverage, built-in tamper evidence,
Power and free (P&F) overhead conveyors use a powered upper chain with pusher dogs to drive unpowered lower trolleys, enabling independent start/stop and accumulation; power-only trolley conveyors run a single continuously moving track with no disengagement. P&F suits multi-station assembly, paint,
Positive discharge bucket elevators handle sticky, sluggish, or wet fragile materials by mechanically inverting buckets at the head, while centrifugal discharge elevators suit free-flowing, durable granules at higher speeds. Choose positive for cohesive fragile loads, centrifugal for abrasive high-t
For elevator buckets, specify polyurethane for sharp, sticky, highly abrasive products, nylon 6 for hot, abrasive service up to 150°C, reinforced nylon for impact-heavy loads up to 170°C, and HDPE for ambient-temperature grain and food where FDA compliance is required.
Plastic pallet capacity ratings assume a uniformly distributed load (UDL); a point or line load on the same pallet can cut effective capacity 40-60% and risk rack failure per ANSI MH16.1.
Pneumatic conveying line routing should favour true vertical and horizontal runs, with each bend sized at 4D to 6D radius to limit pressure drop and elbow wear, and at least 4.5 m (up to 6 m for long-radius bends) of straight pipe kept after the pick-up point to keep saltation velocity stable.
Material test trials before pneumatic conveying system design cut design risk: lab loop, bench rig, and full-scale pilot tests measure conveying velocity, attrition, abrasive wear, and line buildup, each with distinct cost and data output. The 2026 industry consensus ties every dense-phase or long-d
Pneumatic conveying blowers are typically sized in the 5-100 m3/min airflow range at 0.4-2.5 bar(g) for dilute-phase systems, with positive-displacement Roots units dominating below 1 bar(g) and screw compressors used above 2 bar. Sizing requires matching volumetric flow to a target conveying veloci
Plastic pallet static load ratings typically run 15,000–30,000+ lb on flat floor, while dynamic ratings sit 2,000–5,000 lb and racking 1,000–3,000 lb; the ratio is set by ASTM/ISO test methods, not marketing, and the right pick depends on stacking height, forklift impact, and rack-beam spans.
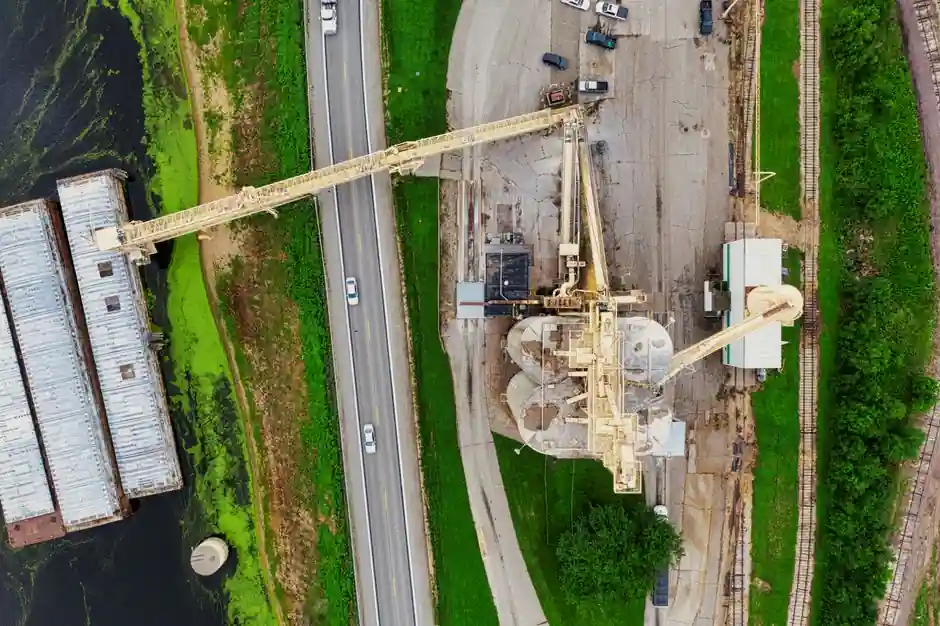
Pivoted-bucket Z-type conveyors keep individual buckets level through both horizontal and vertical runs, while vertical bucket elevators carry rigid, fixed buckets straight up on a belt or chain loop. The defining trade-off is footprint and routing flexibility versus raw vertical lift height and thr
Pit-mounted truck scales save site footprint but cost 20-50% more to install, while above-ground (pitless) scales need ~25 ft approach ramps, are cheaper, and resist corrosion better. Choose pit for tight sites and forklift traffic, pitless for low cost, easy service, and cold-climate frost-line fou
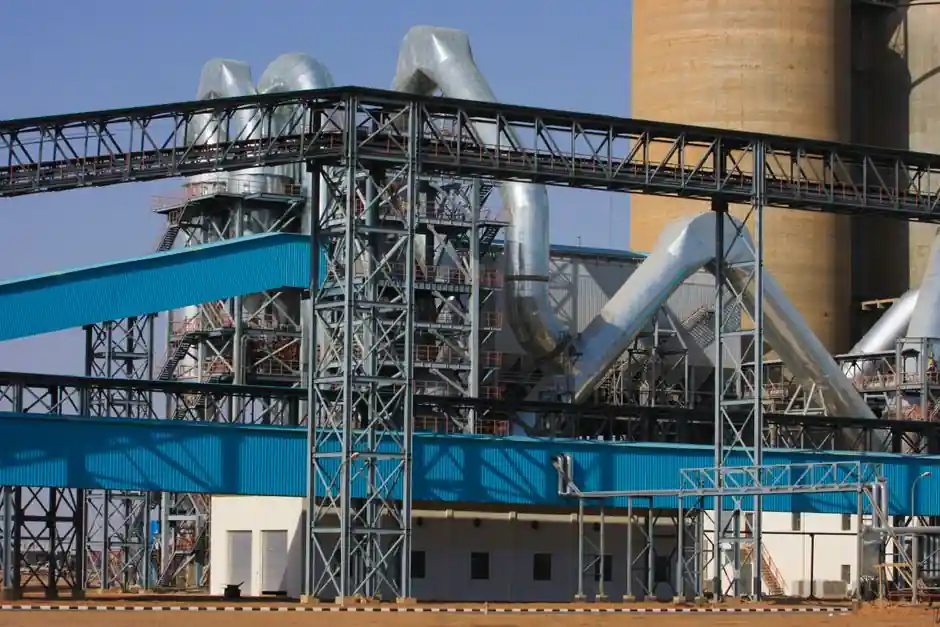
Pipe conveyors carry material in a fully enclosed hexagonal idler tube and handle horizontal plus vertical curves on a single drive, while troughed belt conveyors deliver the highest mass flow of any belt type but stay near-straight unless transfer towers or horizontal-curve designs are added. For c
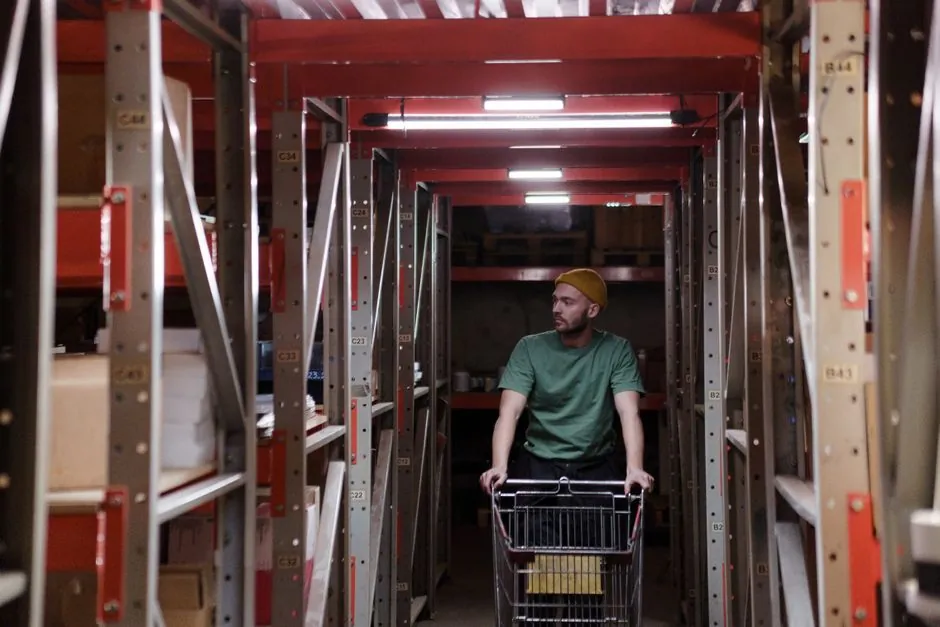
Aisle width in a selective pallet rack layout is set by the forklift, not the rack. Sit-down counterbalances need about 12 ft, reach trucks about 9 ft, VNA trucks 4-7 ft, measured load to load. Layout must also cover flue space, sprinkler clearances, NFPA/OSHA, and bay sizing from the pallet.
Body-in-white (BIW) overhead conveyor trolleys typically span 250 kg light components to 3,000 kg full bodies, with special EMS designs reaching 7 t. Carrier selection is driven by payload, accumulation needs, and oven temperature class rather than speed alone.
For paint line accumulation, power-and-free (P&F) overhead conveyors outperform continuous-flow monorails by letting carriers stop, queue, and release independently without halting the line. P&F typically costs 20-30% less than electrified monorail (EMS) yet handles 5-20,000 lb loads, suits zero-def
For overhead conveyor track selection, enclosed track profiles outperform I-beam rails in cleanliness, curve radius (12–24 in vs 24–48 in) and noise, while I-beam offers lower first cost and up to 10,000 lb capacity. Choose enclosed track for paint, food and pharmaceutical lines; choose I-beam (S3 x
Open order picker platforms maximize reach and pick speed for boxed or bulky SKUs, while three-sided mesh or strap cage enclosures are the safer default for case picking above 1.8 m. Match platform to load profile: aluminum open decks for low-height, high-volume; steel caged decks when fall-object o
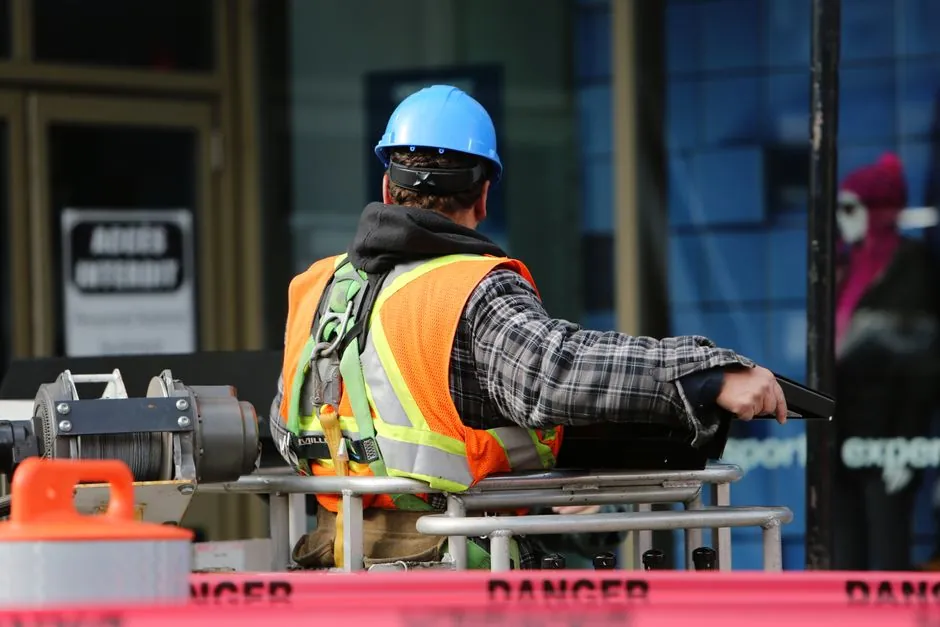
Mid-level order pickers (operators working above 4 ft / generally above 6 ft) require a full-body fall arrest harness with a self-retracting lanyard tied to the truck's engineered overhead anchor, per 29 CFR 1910.140 and 1910.28. The D-ring sits at center back near shoulder level, the anchor must ho
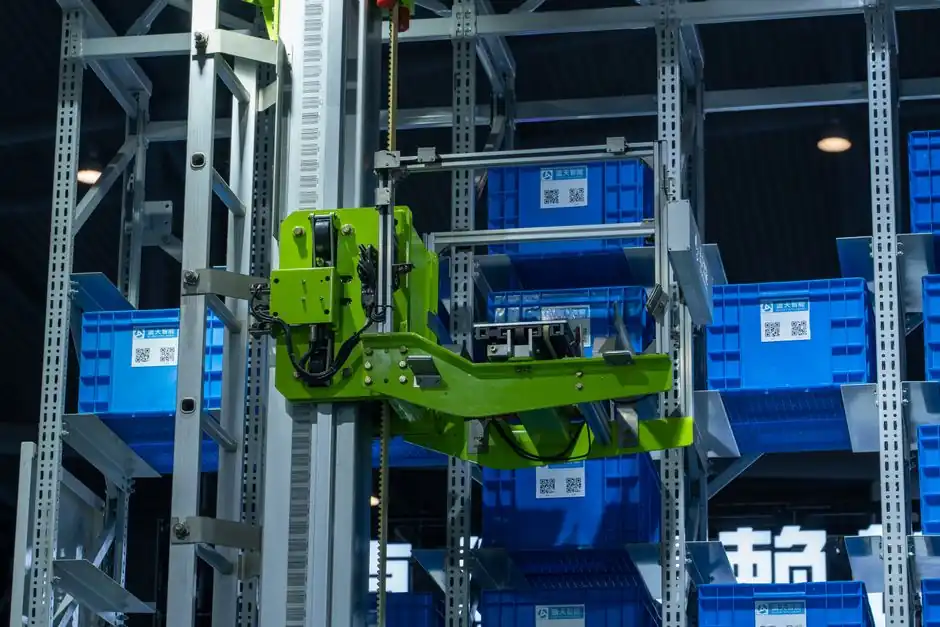
2026 order picker models pair lithium-ion power with telematics as standard fitment: lift heights reach 390 inches, 36V LiFePO4 packs deliver 7.5 mph laden travel, and 8 to 10 hour runtime targets dominate new specs across Toyota, Jungheinrich, Hangcha and TCM line-ups.
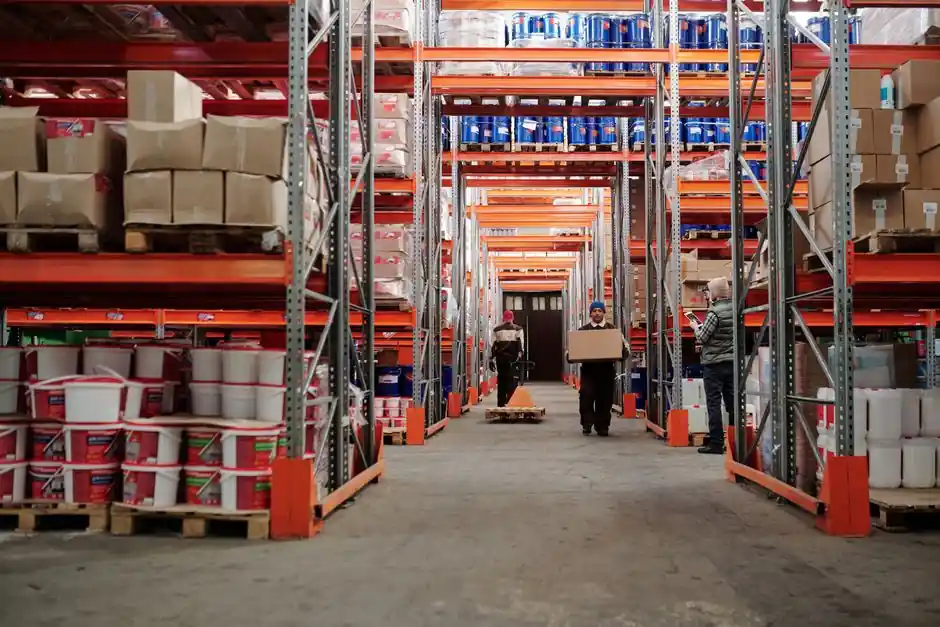
Low-level order pickers typically sustain 80–200 lines per hour, while mid-level order pickers run 40–90 lines per hour because of added vertical travel and lift/descend cycles, per 2026 benchmark data. Specification should be driven by pick-face height, SKU mix, and travel-time share, not raw throu
An order picker with collapsed mast height under 2.4 m is the practical threshold for passing through 2.5 m doors, leaving 100 mm of clearance for tilt and accessories. Triplex full-free-lift masts, not standard 2-stage masts, are the realistic option when both low-door access and 3-4 m picking reac
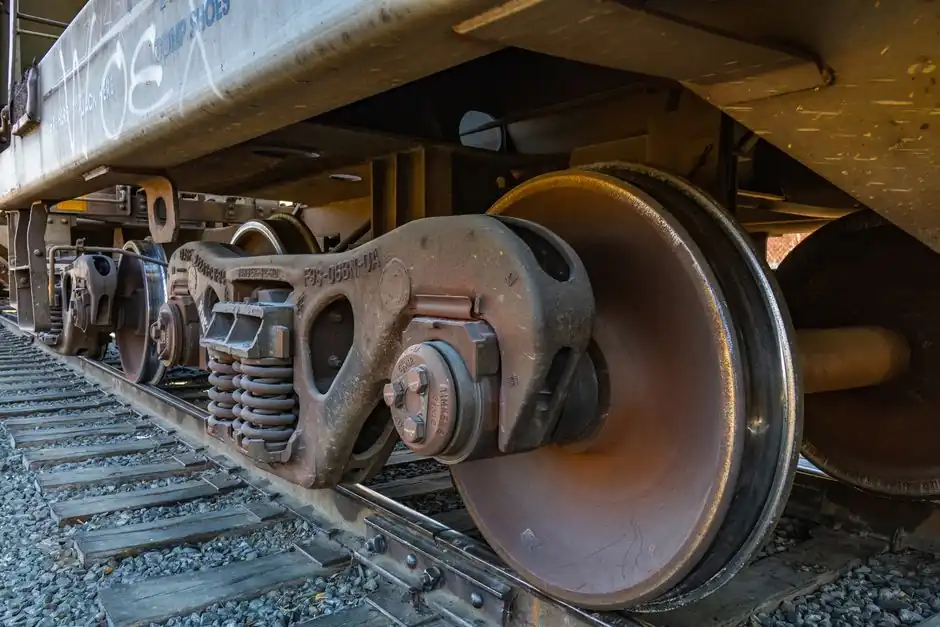
NIST Handbook 44 (2026 edition) assigns vehicle scales to accuracy Class III L, with maintenance tolerance tied to gross vehicle weight, typically 0.1% of GVW or roughly 100 lb at a 100 000 lb loaded rig, applied as acceptance for commerce.
Nestable, stackable, and rackable plastic pallets are three distinct designs: nestable pallets save up to 4× the empty-pallet storage space and cost 50–80% less than stackable units, stackable pallets handle double-stacked loads via solid bottom platforms, and rackable pallets add reinforced runners
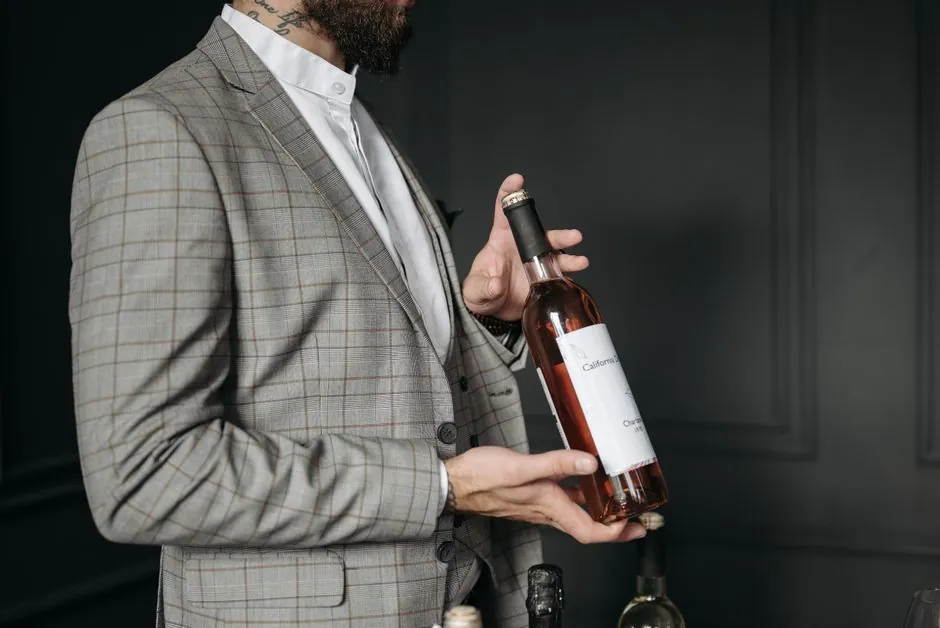
On a 750ml wine bottle, neck labels measure 1.5-3 in wide by 0.5-1.5 in tall and must align rotationally with the front panel; misalignment stems from skipping the tapered-neck sample step, not from the artwork itself.
Modular steel deck truck scales install in 1 day and weigh far less, making them the pick for fast deployment, relocation, and low-profile pits. Full steel deck scales suit heavy, fixed traffic with concrete-grade durability.
Miniload stacker cranes with dual load handling devices double the per-cycle pick rate by extracting two totes in a single S-curve move, with DELIECN's 300 kg class and 180–360 m/min travel range, Daifuku's side-hook extractor, and KAPELOU's 35 kg / 2 m/s spec as the main data anchors[S
Miniload stacker cranes handle totes and cartons under 100 lb at 2-4 m/s in narrow aisles up to 40 m tall; unit-load stacker cranes move 550-2,500 kg pallets at 3-4 m/s with 1.1-1.65 t permitted loads per single-mast class. Pick the miniload for SKU-dense piece picking, the unit-load crane for palle
Medium-level order picker platform heights span roughly 2.8 m to 12.1 m across major OEM lines, with 6 m to 7.5 m as the dense mid-band for 1.0 to 1.25 t class trucks. Sourcing decisions hinge on picking height, capacity, and aisle class, not just the headline lift number.
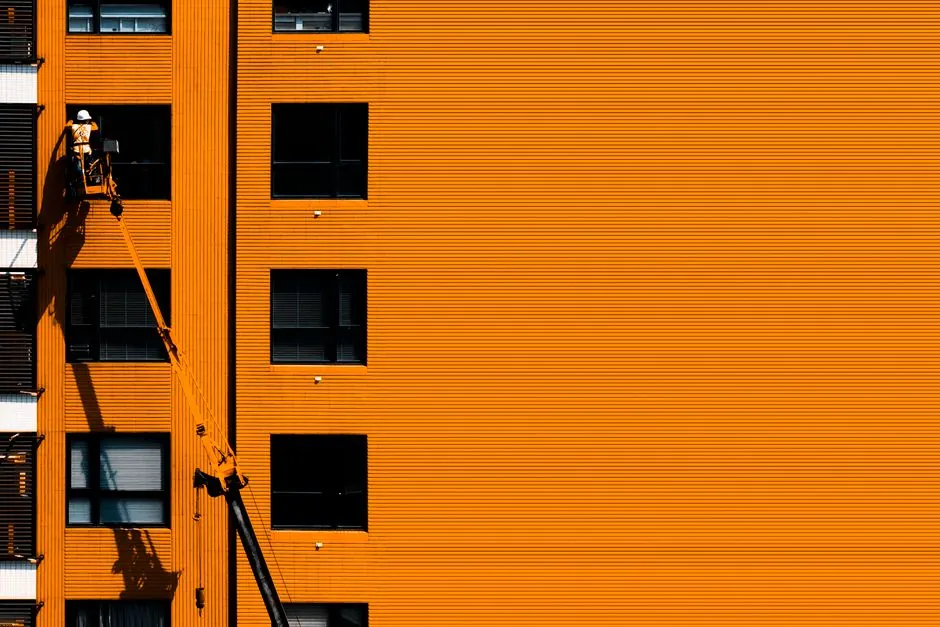
Medium-level order pickers lift operators to rack heights of 3.5–4 m and reach roughly 100–180 picks per hour, while rolling ladders cap out near 60–100 picks/hour at floor-to-low-beam positions. Vertical-man-to-goods picking cuts travel time, which is the dominant 50%+ share of total pick-cycle cos
Medium-phase pneumatic conveying operates at solid-to-air ratios of 7–13 and consumes more air per ton than dense-phase systems, but less than dilute-phase, with energy per ton typically 2–3× higher than dense-phase at the same throughput. Dense-phase cuts energy demand by carrying 20–400× more soli
Dense phase pneumatic conveying moves material at 100 kPa+ in slugs below saltation velocity, dilute phase suspends particles at 700-1,000 m/min (exceeding 5,000 ft/min in many lines), and medium phase sits between. Pick dense phase for abrasive, friable, or moisture-sensitive bulk solids over long
Medium-phase pneumatic conveying typically operates between 5 and 12 m/s air velocity at up to 2 bar gauge line pressure, straddling dilute-phase and dense-phase regimes for 1 to 50 t/h bulk solids transfer over moderate distances.
Medium-phase pneumatic conveying operates between dilute and dense modes, with air velocity typically 600–2,500 ft/min and solids loading ratio in the 15–20 range, requiring careful control to avoid unstable strand flow.
Mechanical pull-chain dock levelers win on upfront price and 110V-free simplicity; hydraulic push-button units win on operator strain, cycle time, and 6x lower lifetime repair cost per Rite-Hite data. Choose mechanical under ~5 cycles/day, hydraulic above that, both for fleets 20,000-80,000 lb.
Manual push trolleys suit loads up to ~250 lb on short runs under 25 FPM with zero electrical cost, while motor-driven overhead conveyors are required once synchronized takt time, lengths beyond 700-800 ft per drive, or 200-1200 lb per hook ratings are specified. Choose push for low-volume cells; ch
For manual pallet jack load and steer wheels, polyurethane wins on smooth indoor floors (quieter, non-marking, better shock absorption) while nylon wins on rough, wet, cold or debris-laden surfaces (higher load capacity, tougher, more chemical and water resistant). Standard 5,000–5,500 lb capacity t
Standard manual pallet jack forks run 36 to 48 in (1150 to 1220 mm) long, with a 27 in overall fork spread and a 3 to 3.5 in minimum fork height, while low-profile variants drop the lowered fork height to roughly 1.5 to 2 in for ground-hugging skids. Pick standard forks for GMA 48x40 in pallets and
A pallet jack scale adds an NTEP-approved weighing system to a standard manual pallet jack, raising upfront cost while letting one operator weigh and move 5,000 lb loads in one pass. Choose the scale model when inbound/outbound verification or legal-for-trade billing is in scope; stick with the stan
A quick-lift (fast-lift) manual pallet jack reaches the pallet in roughly one pump stroke by using a two-stage hydraulic pump, cutting initial handle strokes by about 70% versus a standard single-stage pump at the same handle effort.
Manual pallet jacks for Euro pallets (800 x 1200mm) need forks about 540mm wide across, while North American GMA/CHEP pallets (1000 x 1200mm or 48 x 40 in) require a 27-inch (~685mm) overall width. A 540 x 1150mm truck is the most universal compromise for mixed fleets.
Manual overhead conveyors max out around 50 lbs per operator for sustained horizontal push; once individual carrier loads exceed 250 lbs on enclosed track or 471 lbs/ft on 5 ft centers, the system crosses into the power-assist or fully motorized range. Selection pivots on track style, hanger spacing
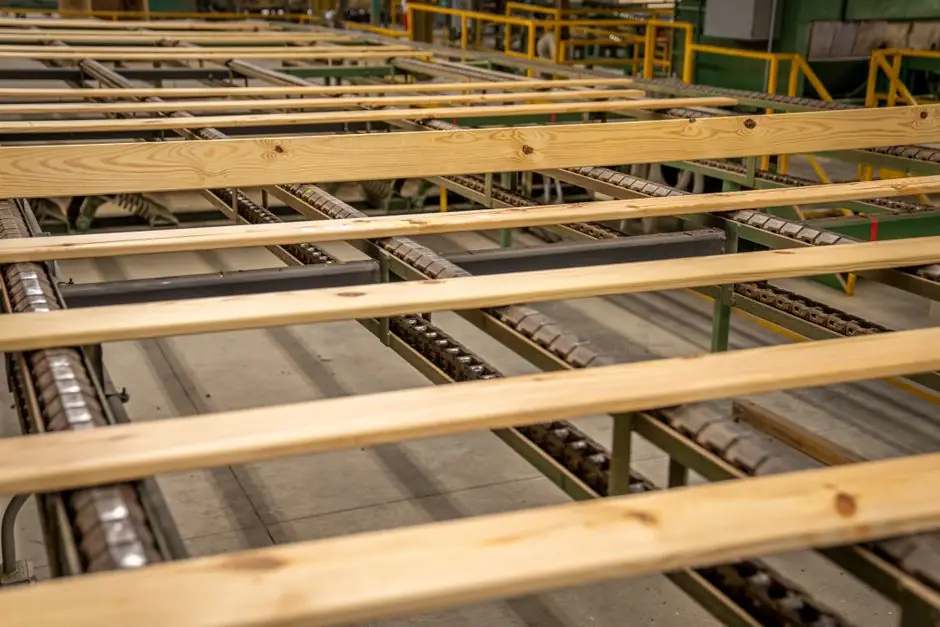
Manual overhead conveyors with gravity-assisted slope run loads up to 4,410 lbs without motors, using 5°+ inclines on enclosed track or I-beam rails. Skatewheel-style trolleys need shallower grades than roller conveyor variants, and common chain pitches span 150–350 mm with 90°/45° curves.
Magnetic-tape-guided AGVs cost less per meter of path and hold line accuracy on a fixed route, while QR-code vision-guided AGVs deliver flexible reroute capability and faster layout changes at higher per-vehicle cost. Choose tape for stable, repetitive loops under 100 m; choose QR for mixed-SKU orde
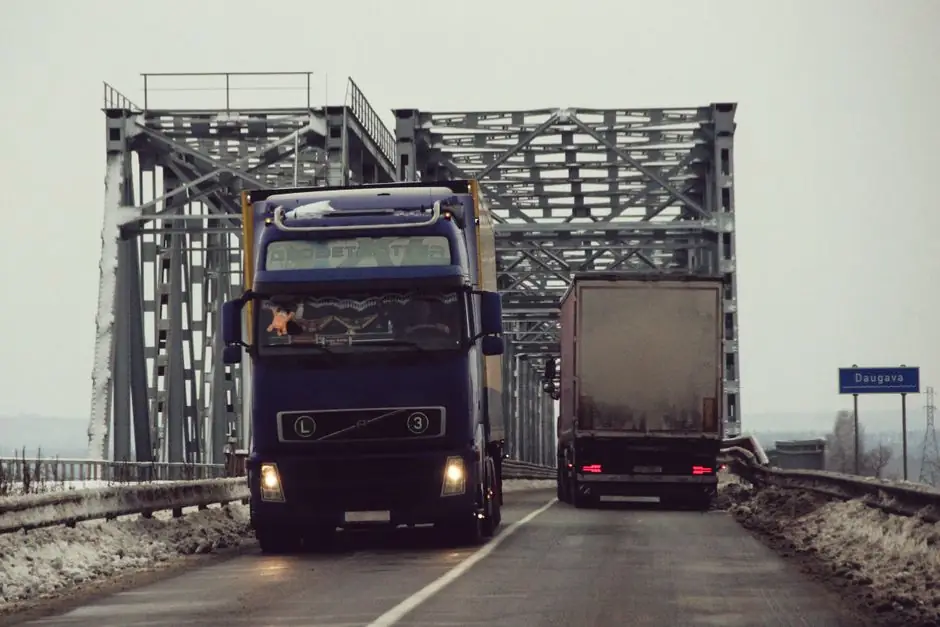
Low-profile and standard-height pitless truck scales both install above grade, but the low-profile version drops the approach ramp to roughly one vehicle tire revolution, while a standard pitless unit typically stands 28-51 cm (11-20 in) tall and needs 140 ft of clearance for a 70 ft platform. Choos
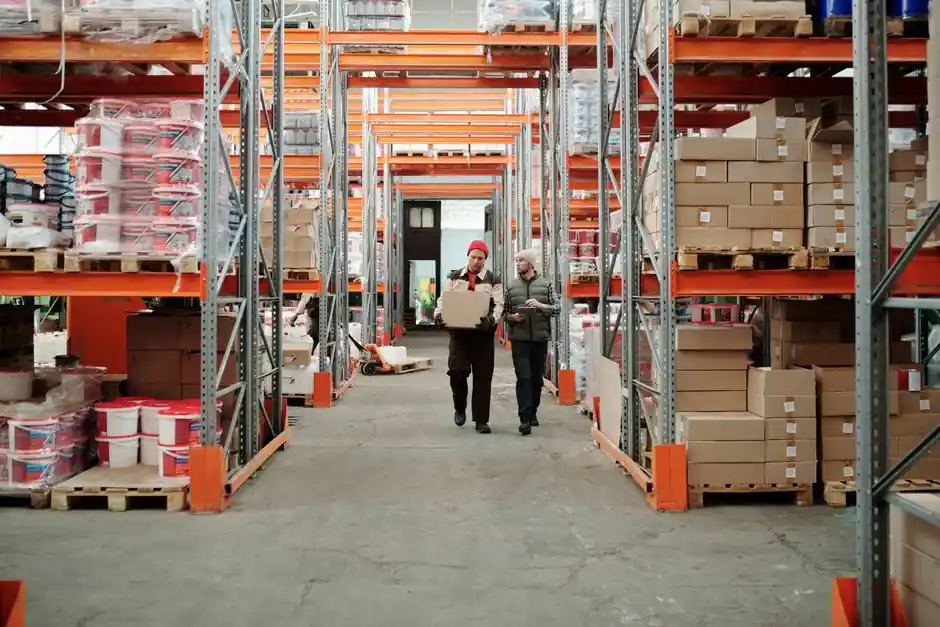
Low-level order pickers (LLOPs) handle ground to about 2.5 m picking and are the lowest-cost option; medium-level pickers cover roughly 2.5 to 6 m; high-level / VNA man-up pickers reach 12 m, with operator-up platforms documented up to 40 ft (about 12.2 m). Match the picker class to rack height, ais
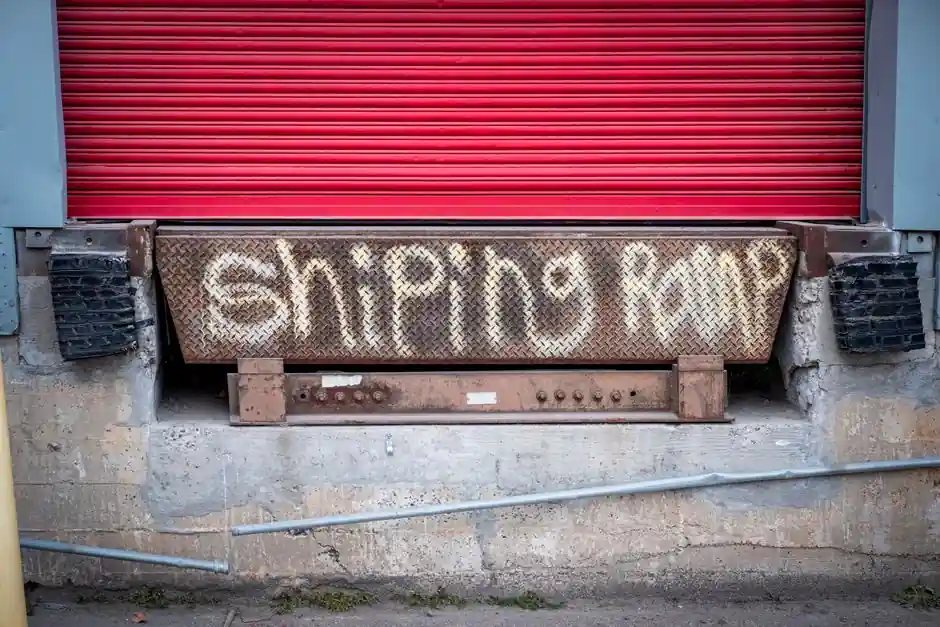
Embedded steel angle coping for a pit or edge-of-dock leveler is typically a 3" x 3" structural section with rebar mud hooks welded to the back, set flush with the finished floor. Older docks without this embedment need a 1/4" steel approach plate retrofit because EOD units must be welded, not just
Recessed dock leveler pits require a 25-30 mm drainage slot or weep hole at the lowest point of the pit floor, sloped at roughly 1:50 toward a trapped floor drain, to prevent standing water that freezes and heaves the frame. Frost-susceptible sites additionally need a 100-150 mm extruded polystyrene
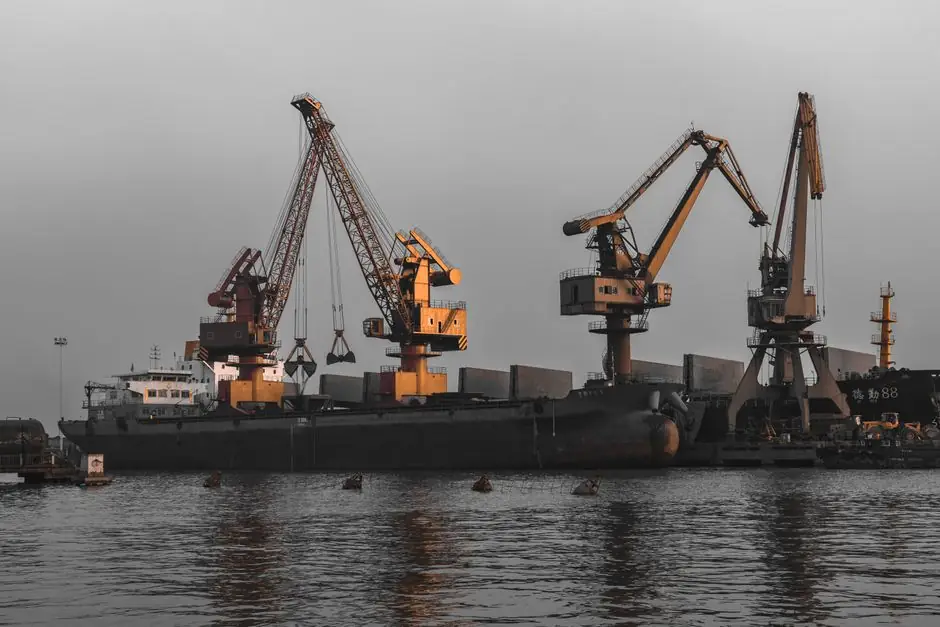
For stacker cranes, telescopic forks dominate single-, double-, and triple-deep pallet AS/RS with travel speeds up to 240 m/min and 1.65 t max load, while shuttle forks (telescopic slides on rail-guided carriers) win on cube density for high-throughput box handling. Pick telescopic for height + FIFO
A live bottom multiple screw feeder uses two or more parallel screws as the floor of a straight-sided bin, drawing material evenly across the full outlet width to defeat bridging. Selection hinges on variable-speed drives, flooded inlet design, and tapered geometry matched to the specific bulk solid
Light-duty stacker cranes (≤1 ton) are widely specified for e-commerce, retail and small-pallet AS/RS, while heavy-duty units (≥5 tons) dominate industrial segments, per August 2026 market segmentation. Selection should follow unit-load weight, lift height, aisle width and throughput, not r
Tamp-blow labelers deliver contactless, vacuum-and-air placement for small labels on irregular or recessed surfaces, while wipe-on applicators use direct contact pressure and require product speed synchronisation. Tamp-blow is the default for variable-height products, restricted access zones, and pr
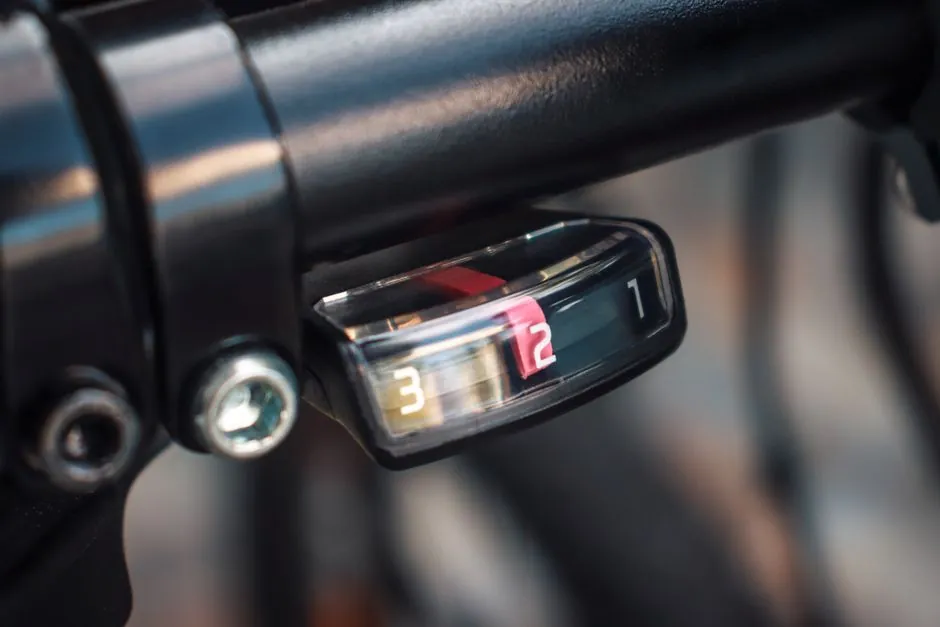
Label sensor and dispense edge are the two subassemblies that determine registration accuracy on pressure-sensitive labelers. Ultrasonic, optical, capacitive fork, and retro-reflective sensors cover different label/liner combinations, and the peel-tip geometry dictates placement repeatability on cyl
ISO 8611-1:2025 sets the static bending, compression and creep test methods for flat pallets, while ISO/TS 8611-4:2013 provides the regression-based shortcut to predict 1.5–2% deflection limits and shorten full-load test duration on plastic pallets.
EN ISO 3691-4:2023 supersedes EN 1525:1997 and defines a Type C safety regime (per EN ISO 12100) for driverless industrial trucks, covering zones, hazards, and safety functions. Use ISO 3691-4 for new AGV/AGC deployments; EN 1525 only persists for legacy equipment already on the EU market before wit
ISO 21898:2024 (published September 2024, supersedes the 2004 edition withdrawn 2024-08-16) governs flexible intermediate bulk containers for non-dangerous solid materials in powder, granular or paste form, and replaces EN ISO 21898:2005 across CEN member states by March 2025.
Structural pallet rack costs more per pallet position than roll-formed, but pays back in freezer, wash-down, and high-impact aisles where dented columns become a maintenance liability. Roll-formed teardrop is the correct default everywhere else, given lower cost, faster install, and easier re-pitchi
Precast concrete decks win on portability and install speed, while site-poured concrete decks win on traction, mass, and deck life. For most permanent truck scale sites, a site-poured concrete deck outperforms a precast deck; for temporary or relocatable sites, steel or precast typically makes more
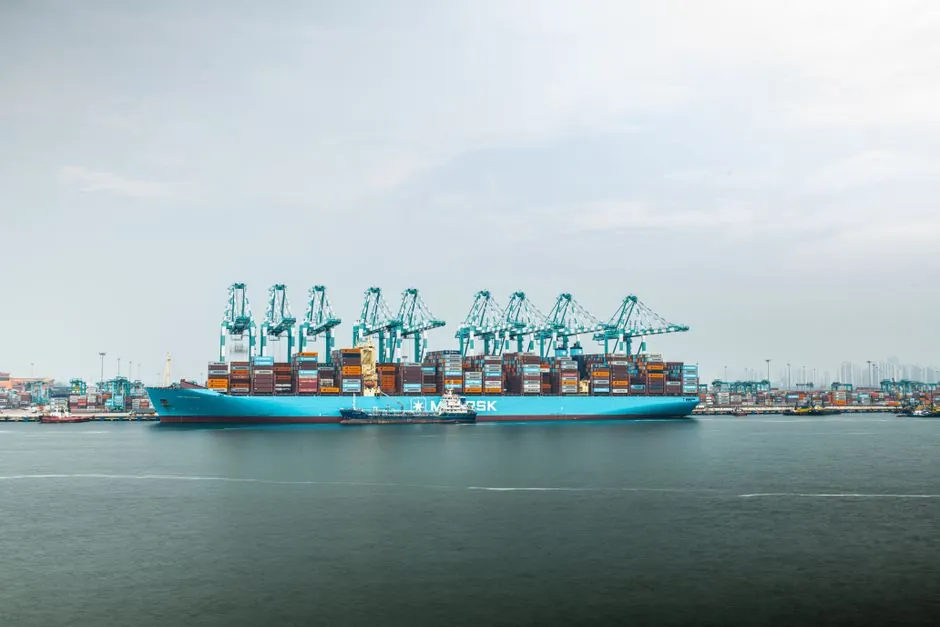
Export crates for heavy machinery typically use 1.25 in (32 mm) PET or steel strapping as the baseline, with 1.5 in to 2 in steel reserved for loads above 5,000 lb or with sharp edges. Selection follows load weight, edge risk, strap path, and FMCSA securement rules.
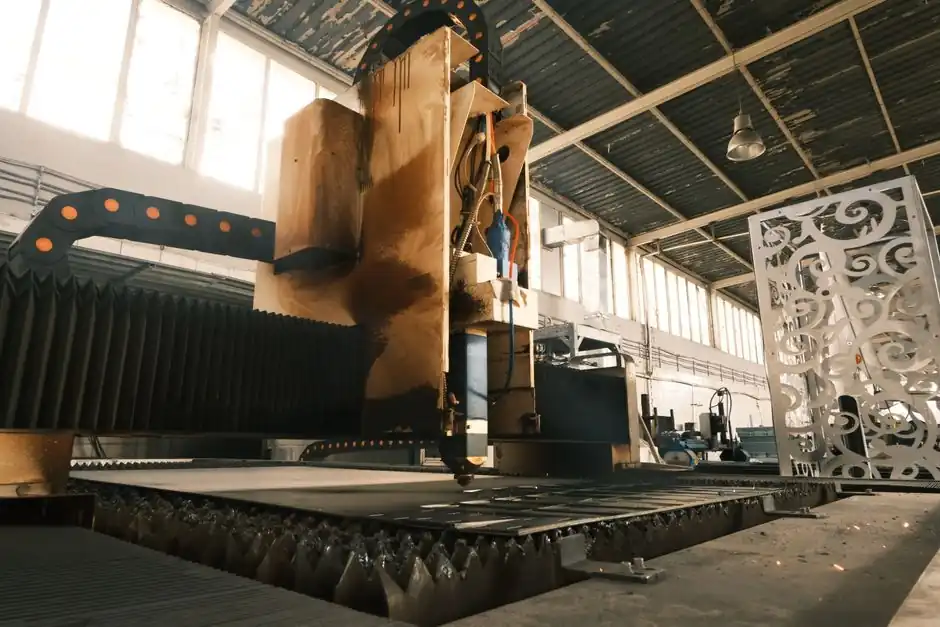
Industrial AGV payload spans 50 kg light-duty units to 600-ton heavy-duty platforms as of 2026, with the 500–2,000 kg band covering most warehouse and pallet work. Selection hinges on load class, drive type, and navigation technology rather than headline capacity alone.
In-mold labeling (IML) fuses a pre-printed label into the plastic during the molding cycle, eliminating the post-mold labeling (PML) step entirely; PML applies pressure-sensitive or sleeve labels after the container is formed.
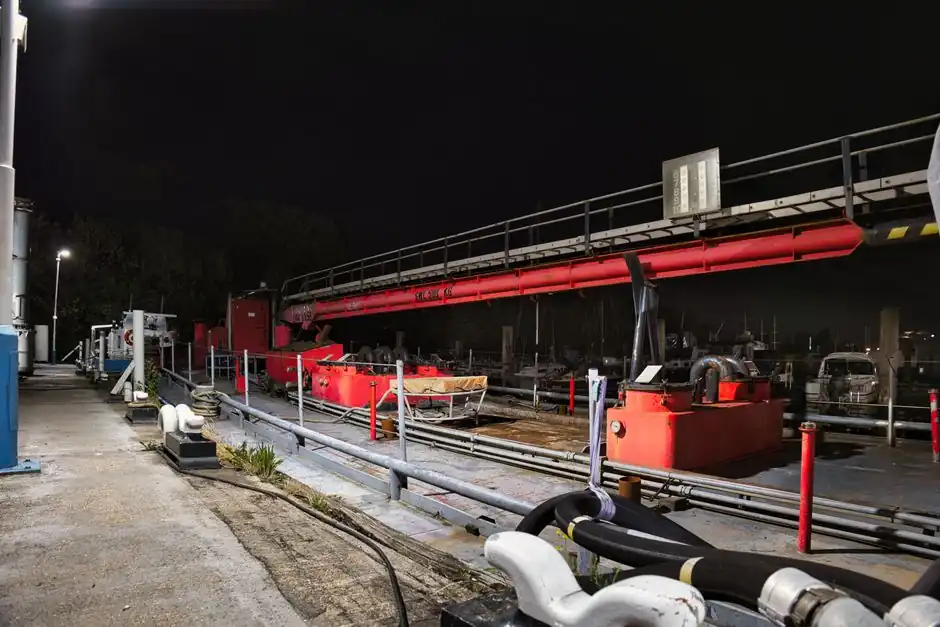
Hydraulic dock levelers deliver higher capacity and lower lifetime cost for heavy, high-cycle use, while air-powered dock levelers trade capacity for lower first cost and simpler maintenance on low-volume docks. Pentalift and Nosteclift both state hydraulic units are ideal for heavy-duty application
A four-strap pallet configuration needs roughly 1.5× total break-strength across all bands (per-strap rating = pallet weight × 1.5 ÷ 4), with PP strap needing the most linear footage per loop due to elongation loss, and steel needing the least. For a typical 48×40 GMA pallet, plan ~14–22 ft of strap
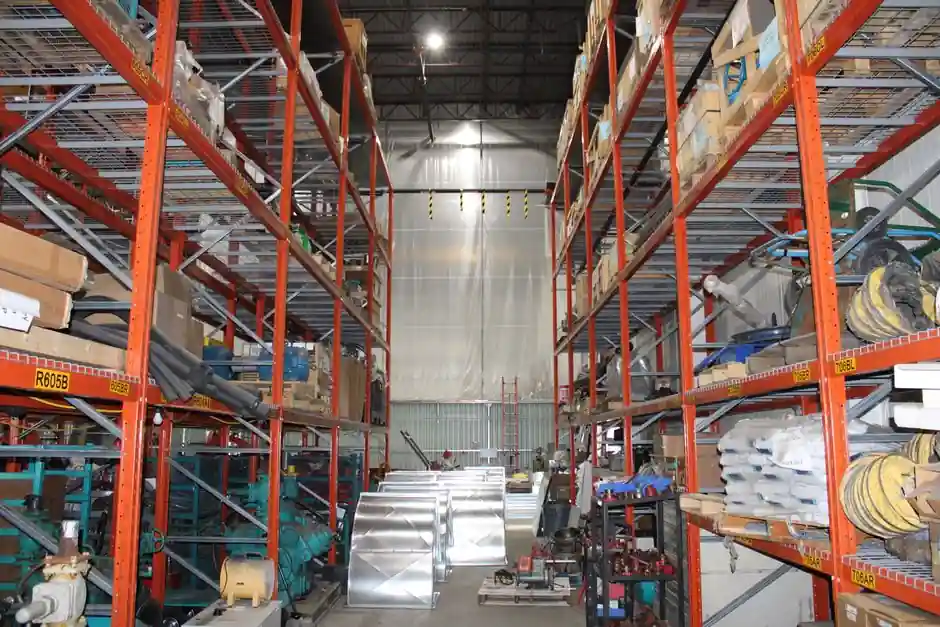
Mobile pallet racking delivers roughly 80% to 200% more pallet positions than selective racking inside the same footprint by collapsing fixed aisles into one moving aisle, with common benchmark gains of about double the storage density.
A single 90-degree bend in pneumatic conveying pipework adds roughly 5 to 12 m of equivalent straight pipe, with long-radius (8D-14D) bends at the low end and short-radius elbows at the high end. Pre-project shortcuts use a flat 5 m per bend; detail design uses radius- and angle-specific values from
Regenerative braking on a stacker crane recovers 20-40% of braking energy under typical duty, with one OEM solution claiming up to 50% total system reduction when paired with cycle-optimised software. Real savings depend on lift height, travel speed, and load profile.
One vertical lift module typically replaces 6 to 12 rows of static shelving in a 25-foot-clear warehouse, freeing up to 85% of floor space and lifting pick rates to roughly 4× the static-shelving baseline of about 60 picks per hour.
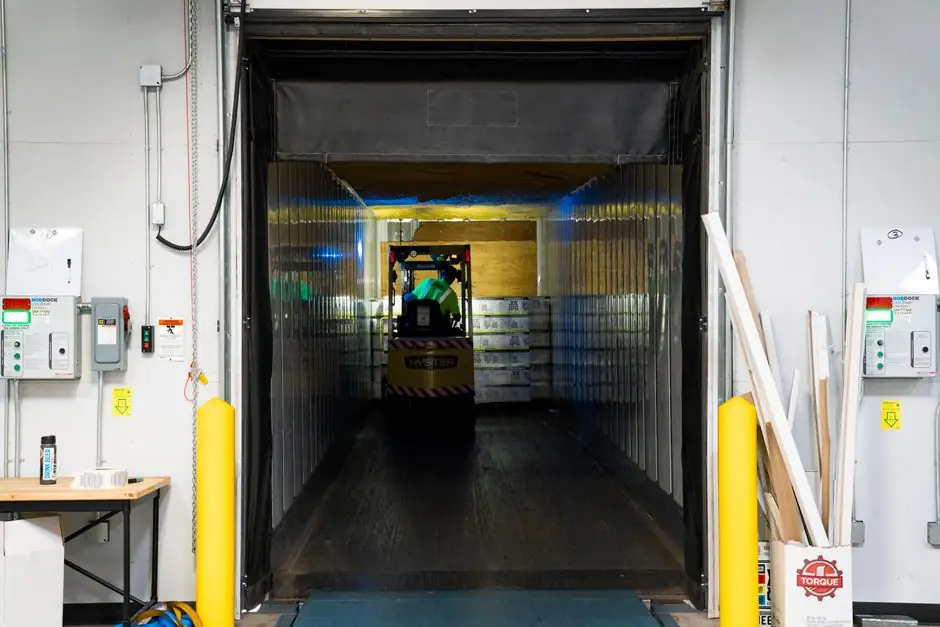
A new exterior-mount dock leveler can be installed in 1-2 days per door, a pit-style hydraulic replacement takes 1-2 days of crew work after pit prep, and full new-pit projects run 4-6 weeks of facility downtime. Plan lead time, crew mix, and dock door count before scheduling.
Modern single-mast stacker cranes travel up to 160 m/min unloaded and hoist at 66 m/min unloaded (54 m/min loaded), with combined-axis motion driven by the WCS to compress cycle time. Realistic aisle throughput lands in the 30-60+ dual-command cycles/hour band for pallet AS/RS, versus 200-1,000+ mov
Load swing penalises overhead conveyor trolley capacity by forcing conservative derating of static ratings, typically reducing usable per-carrier load by 20-40% on I-beam monorail runs above 100 FPM. Heavy parts above 250 lb and high ambient temperatures (paint bake up to 220 °C) demand dual-pendant
Dual-tray delivery on a Vertical Lift Module (VLM) removes operator wait time by staging the next tray behind a shutter while the current one is picked, overlapping transport and pick windows. White Systems' Compact Double and Kardex Shuttle XP use this dual-tray principle to collapse dead minutes p
A VLM extractor is a single vertical elevator that rides the center column of an enclosed tray stack, grips the requested tray, and delivers it to a waist-height access opening in seconds. The same mechanism, often called the inserter/extractor, also returns trays to storage and uses a laser height
A stacker crane retrieves pallets from a storage rack through three coordinated motion axes (horizontal travel, vertical lift, and telescopic fork extension), reaching up to 45 m high in aisles as narrow as 1.5 m wide at 30-60 pallet moves per hour per aisle.
A roller-conveyor gate interlock is a safety switch wired in series with the drive-motor contactor or variable-frequency drive enable circuit. When the gate opens, the interlock breaks the enable, the drive drops out, and the rollers coast to zero before a worker can reach the nip point.
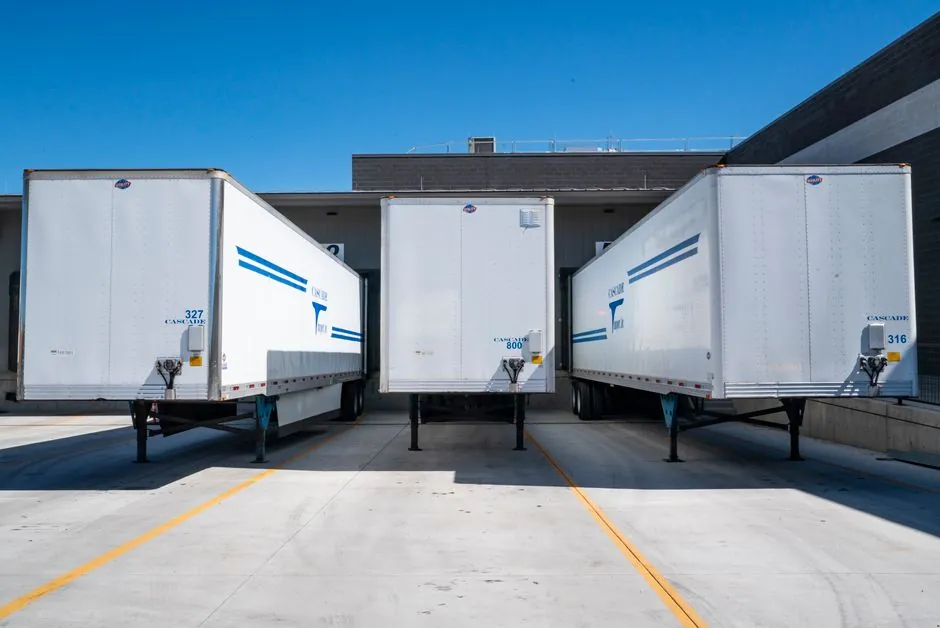
A dock leveler is a steel or aluminum platform that bridges the typical 8-10 inch gap and 12 inch up/down height swing between a fixed 48 inch dock and a 36-60 inch trailer bed, using a hydraulic cylinder, air bladder, or spring to raise the deck, extend a hinged lip onto the truck, and float with t
For a 10-cell truck scale, divide the maximum gross vehicle weight by 10, then apply a 1.5 to 2.0 safety factor and a 1.2 to 1.5 dynamic-impact factor so each cell is sized for roughly 15 to 30 percent of truck GVW. Double-ended shear beams (1,000 to 200,000 lb) and canisters (20,000 to 500,000 lb)
Pipeline diameter in a pneumatic conveying system is set by three coupled choices: conveying mode (dilute vs dense), material saltation velocity, and required mass throughput, with the final bore derived from the continuity equation Q = v × A at a target gas velocity 20-30% above saltation. Typical
Bucket elevator capacity in t/h is calculated as: Capacity (t/h) = (V × ρ × S × 60) / D, where V is bucket volume, ρ is bulk density, S is belt speed, and D is bucket spacing. Centrifugal discharge units run 1.0–2.5 m/s; continuous-discharge units 0.5–1.0 m/s, with fill factors of 0.75 typical for g
Belt conveyor capacity in TPH equals belt speed (ft/min) times load cross-sectional area (ft²) times bulk density (lb/ft³) times 60, divided by 2000. For a 36-inch troughed belt running 300 ft/min at 100 lb/ft³, the calculated throughput is 450 TPH.
Air temperature and site elevation change air density, forcing engineers to derate pneumatic conveying blowers: a standard 20 deg C sea-level ICFM drops roughly 18 percent at 1,500 m and 25 percent at 2,500 m, while inlet air above 40 deg C costs another 6 to 8 percent of mass flow per 10 deg C rise
Hollow-flight screw conveyors heat or cool bulk solids by circulating thermal media through the screw flights and a center pipe, with industrial units operating up to 700°F in carbon steel and up to 1,200°C in high-alloy builds. They suit short-to-medium horizontal conveying with 15–40% trough fill
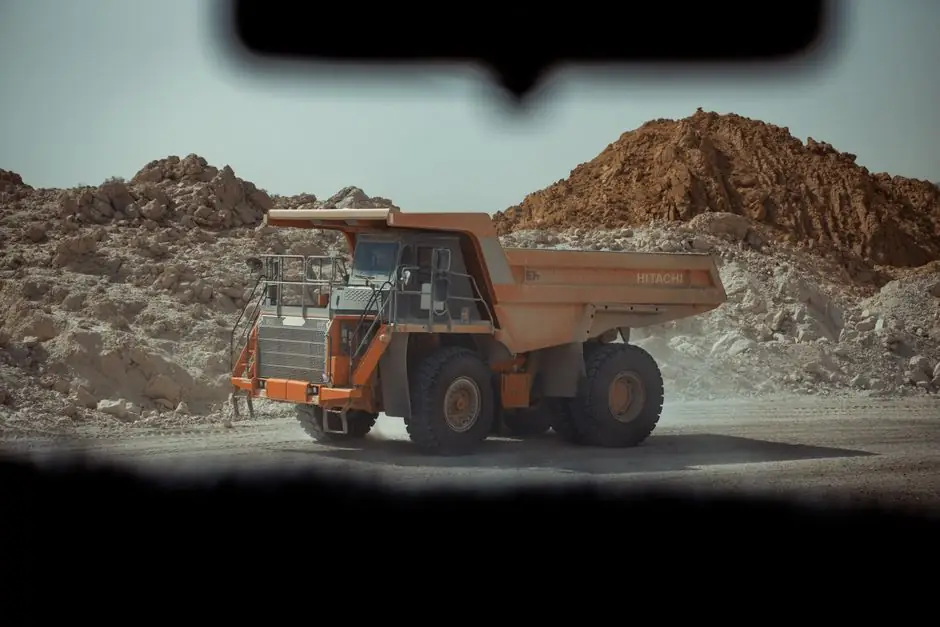
Heavy-load AGVs in the 20 t die and mold transport class are commercially available from multiple suppliers with published payloads from 6 t up to 500 t, with custom-engineered units rated for 30 t static load during automotive mold changeover. Selection hinges on payload, aisle width, navigation ty
Heat transfer labeling equipment decorates plastic containers (PE, PP, PET) using heated silicone dies and pressure to apply multi-color labels, reaching up to 355° coverage on 1-6 gallon pails at 800 cph for 4-liter sizes. Dry, recyclable process favored for food, chemical, and agricultural pails.
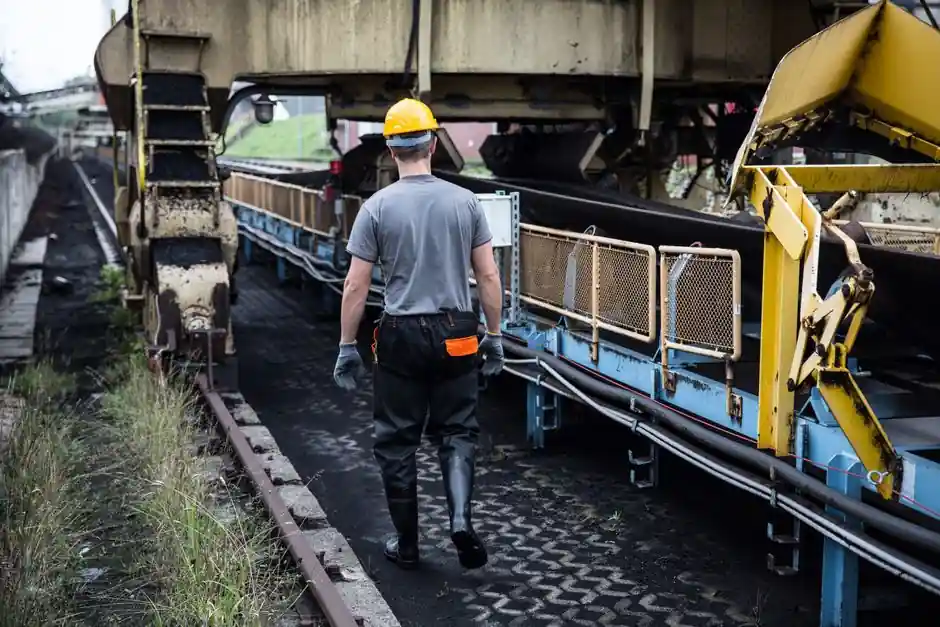
Heat resistant conveyor belts handle material temperatures up to 250°C under DIN 22102, while fire resistant belts are engineered to self-extinguish with average afterflame under 60 seconds per MSHA Schedule 2G. Choose heat resistant grades for hot product service and fire resistant grades for combu
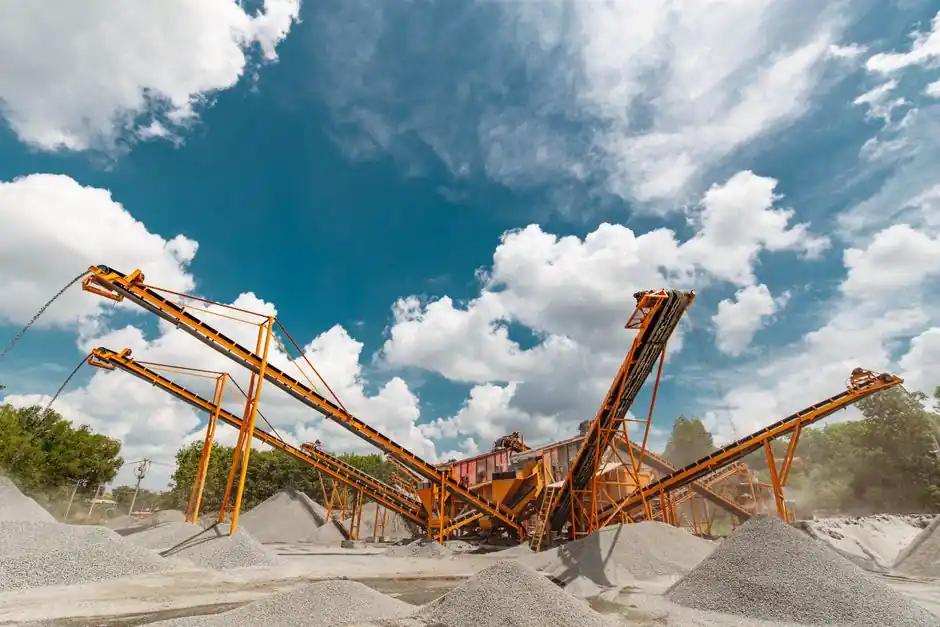
Flared trough screw conveyors widen the top opening versus a standard U-trough to admit sticky, viscous, or bridging bulk solids, and are widely used as mixing conveyors where headroom above the flight is required. Standard CEMA screw diameters run 6 to 24 inches, lengths commonly reach 150 feet, an
FIBC bulk bags are rated by Safe Working Load (SWL, typically 500–2,000 kg) and a Safety Factor (SF) of 5:1 for single-trip or 6:1 for reusable/UN-hazardous use, per ISO 21898. A 1,000 kg SWL bag at 5:1 must withstand 5,000 kg before failure; never load beyond the stated SWL.
FEM 9.851 defines six cycle cases and three load-handling types for stacker cranes, with the double cycle (Doppelspiel) as the canonical throughput metric in DC/h. Cycle time sums constant and variable times from kinematics and distances, while mean energy demand is derived from FEM-defined referenc
EP fabric belts dominate bucket elevators up to about 50 m lift at 50-500 t/h, while steel cord belts take over above 60 m with 0.3% elongation versus 4% on NN fabric. Match carcass to center distance, take-up travel, pulley diameter, and impact zone, not to belt cost alone.
EN 528:2021+A1:2022 is the active European safety standard for rail-dependent storage and retrieval (S/R) machines, superseding EN 528:2008. It covers unit-load, long-goods, and order-picking cranes operating indoors, including aisle transfer equipment, with EMC and noise provisions.
EN 15095:2007+A1:2008 specifies safety requirements for power-operated storage carousels, storage lifts, and mobile racking in scope ICS 53.080, covering mechanical, electrical, and ergonomic hazards under EU Directive 2006/42/EC.
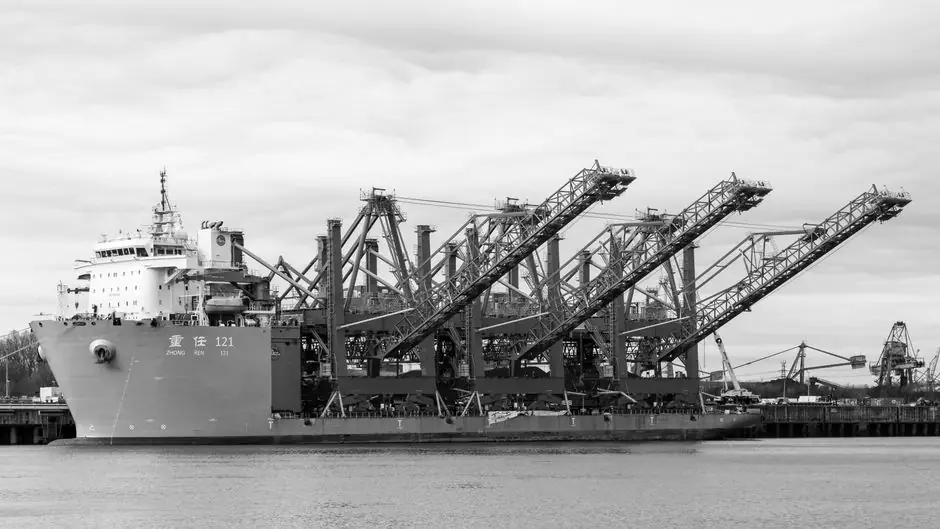
Elevator-type (single-mast) stacker cranes and rail-guided mast stacker cranes both run on floor-rail and upper guide-rail pairs, but differ in mast count, load band, and aisle application. Single-mast units are optimal for lighter loads under 1.65 t, while twin-mast configurations handle heavier or
Edge-of-dock (EOD) levelers install 10x faster than pit-mounted levelers by bolting to the dock face, avoiding the concrete pit work that adds cost and downtime to pit installations. Choose EOD for retrofit projects, light-duty service below 30,000 lb capacity, and uniform 48-50 in. trailer fle
Dual-unwind automatic label splicing lets pressure-sensitive labeling lines run continuously through roll changes by detecting end-of-web, cutting, and butt-joining the new roll in motion. Production units such as the Label-Aire NSDU reach 4,300 in/min on dual 20 in. cores, and are now standard for
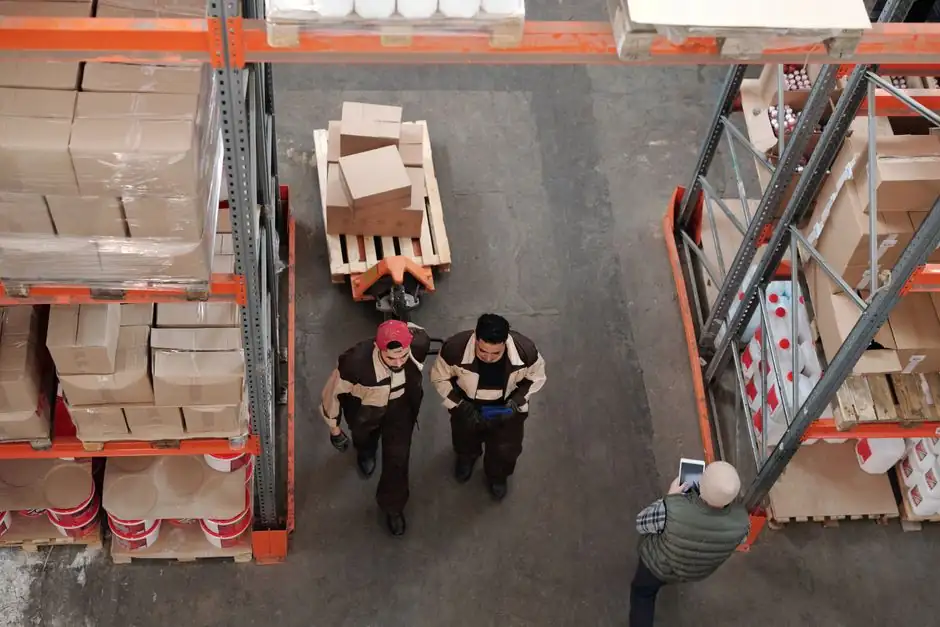
Double-deep pallet racking delivers roughly twice the pallet positions per square foot of selective rack by halving aisle count, but pays for that gain in immediate-access selectivity and forklift specialization. Selective rack remains the right call for mixed-SKU, FIFO operations; double-deep fits
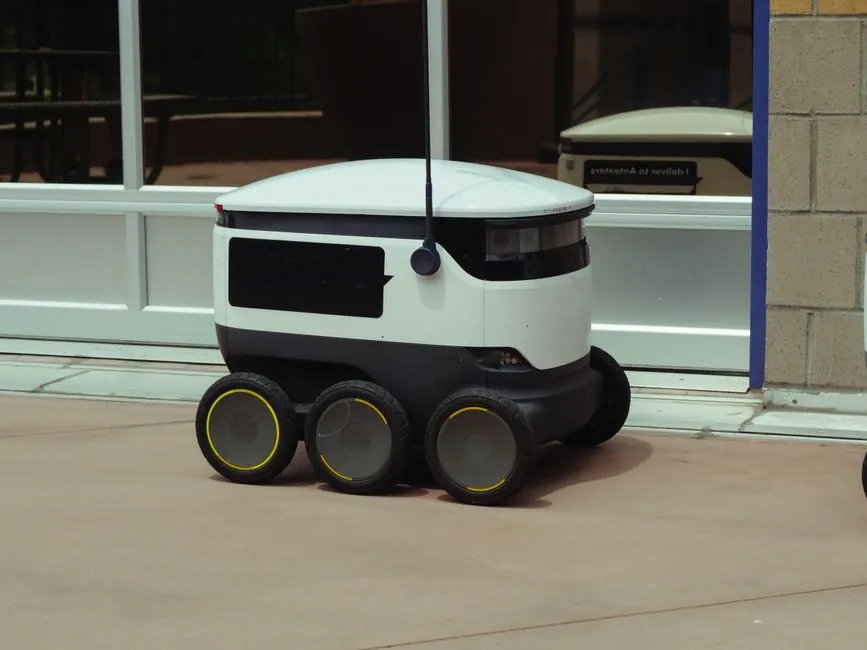
ISO 3691-4 applies directly to autonomous mobile robots (AMRs) and automated guided vehicles (AGVs): the standard's scope explicitly names both as driverless industrial trucks, and the 2023 edition governs detection, zone, and speed requirements for CE marking in the EU.
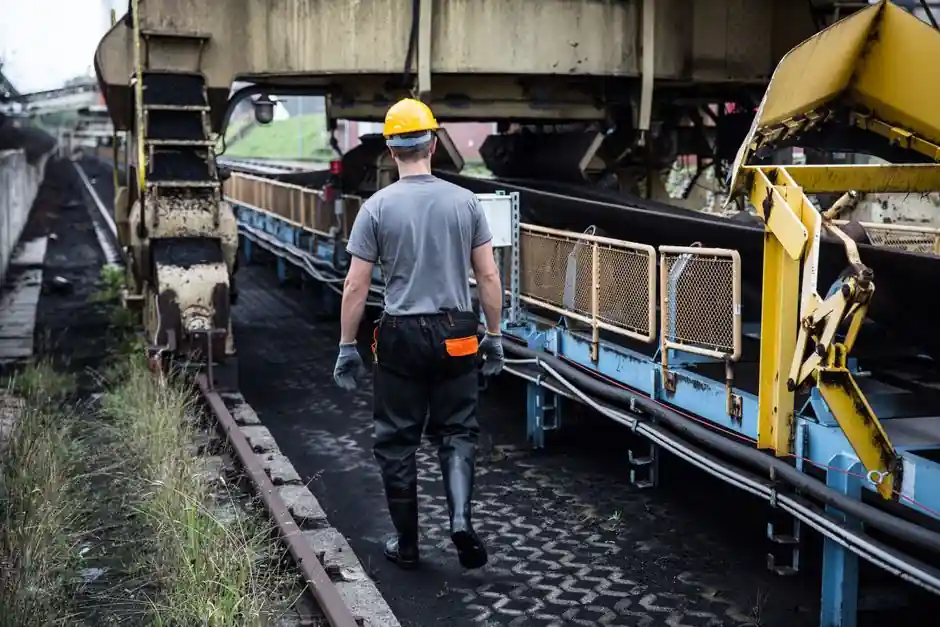
Screw conveyors do damage fragile or friable products by design, and the degree of breakage is controlled by screw diameter, fill level, rotational speed, and trough clearance, not by the conveyor type alone. For low-friability bulk solids a standard screw conveyor can be acceptable; for true friabl
Two-way plastic pallets fit fixed-route, low-repositioning operations and cost less up front, but four-way pallets win in high-throughput, rack-loaded, multi-direction handling environments. Global pallet-handling equipment spend reached $48 billion in 2024, and entry design is now a direct driver o
A pitless truck scale uses a slab foundation, not a pier foundation. Piers support an aboveground weighbridge; a monolithic slab supports a pitless (flush-to-grade) installation, typically requiring 1,500 PSF soil bearing and 24 in. of compacted aggregate base.
Mechanical dock leveler spring tension is set with the adjustment nut at the main spring paddle: clockwise turns increase tension to restore lift, counterclockwise releases it for spring replacement, and the deck must be blocked by a maintenance strut or jack before any work. A 300 lb. pallet is the
Standard dock leveler widths are 6 ft, 6-1/2 ft, and 7 ft, with 6 ft most common; capacities span 35,000–80,000 lbs covering 95% of installations, with dynamic multipliers of 2.0–5.0 over static ratings.
Mechanical and hydraulic pit dock levelers require welded steel shims under the rear frame plus a staged tack-and-stitch weld sequence (rear centre first, then ends, then front keepers) to keep the platform flush with the pit floor and prevent fatigue cracking at hinge tubes.
Dock leveler perimeter brush seals cut under-platform air infiltration by filling the side and rear gaps between the leveler deck and the concrete pit wall, using dense nylon filaments in aluminum or galvanized holders sized to the gap. Specified exposed filament lengths run 0.41" to 5.00" across SE
Standard dock leveler lips come in 16, 18, and 20 inch lengths for full pit style hydraulic and air units, with a 15 inch lip on mechanical edge of dock levelers and a 17 inch option for refrigerated trailers. The lip must reach at least 4 inches into the trailer per ANSI MH30.1, and typically proje
For a recessed dock leveler, pit depth is set by the leveler's subframe height and required working range, while lip length is a separate spec that must clear the pit recess and the truck bed safely. Standard pit length is a minimum of 6 ft, with typical working range of 12 in. above and below dock
Dock leveler deck plates typically use 1/4" to 1/2" thick high-tensile tread plate steel in the 50,000 to 55,000 psi (345 to 379 MPa) yield range, with thickness scaling to capacity (CIR) rating rather than to yield strength. Thicker plate buys fatigue life, but the underlying steel grade governs de
DIN 22102 cover grades W, X, Y, and Z differ in minimum tensile strength, elongation at break, and maximum abrasion loss, with W the most abrasion-resistant (≤90 mm³) and Z the lightest duty (≤250 mm³). Selection hinges on material abrasiveness, lump size, and impact energy at the feed point.
Counterbalance forklifts and reach trucks run on different cost curves per pallet move: counterbalances have lower acquisition cost ($25,000–$45,000 for electric stand-up versions) but demand wider 3.2–3.8 m aisles, while reach trucks ($35,000–$60,000) cut aisle width to 2.7–2.9 m, lifting storage d
For narrow-aisle warehouses, the reach truck beats the counterbalance forklift on aisle footprint (≈2.7–3.0 m vs 3.2–3.8 m) and lift height (12 m+ vs ≈5 m), while the counterbalance wins on versatility, load capacity (1,500–5,000+ kg) and outdoor use. Match machine to aisle width, lift height, load
Conveyor specification starts with three material-driven inputs: bulk density, lump size, and lift geometry. Sizing a belt conveyor or screw conveyor without measured density, largest-lump dimension, and incline profile produces overloads, plugging, and premature wear.
Cross-belt and loop sortation systems deliver 9,000 to 27,000 items per hour at the high end, while top-tier distribution centers push 40,000 to 50,000 sorts per hour. Throughput hinges on sorter class, induction rate, and destination count, not loop speed alone.
Singulation-stage induction sets the ceiling on any sorting system: the sorter itself rarely bottlenecks. On paired singulator-plus-induction builds like the Fives SOLI-Modular, feed to the sorter exceeds 4,000 parcels per hour, and cross-belt carriers are the usual high-rate sink. Below that, rate
At 35° troughing with three equal-length rolls, a CEMA standard belt carries roughly 27% more cross-sectional area than at 20°, and a 600 mm belt at 35° carries ~30% more load than the same belt at 20°.
Plied conveyor belts are built from top cover, fabric carcass plies (1-6), skim coats, and a bottom cover, with the top cover typically 3:1 thicker than the bottom and 30-50% of total belt thickness. Excessively thin covers force premature carcass shock load; excessively thick covers raise bending s
For automated stacker cranes, insulated conductor rail is the default electrification when run length exceeds roughly 60 m, duty cycle is high, or the aisle has no room for cable loops. Festoon cable remains the lowest-cost option for short, light-duty bridges under 30 m where moderate sag is accept
Chain conveyor load handling devices on stacker cranes and telescopic forks are both pallet AS/RS extractors, but the chain conveyor is a direct pallet-transfer attachment sized for order-picking discharge onto live conveyor lines, while the telescopic fork is a stroke-extension tool for single/doub
Centrifugal-discharge bucket elevators run fast (typically 225–300 fpm belt speed) and are the fit for free-flowing, durable bulk solids; continuous-discharge units run slow, are gentler on fragile/abrasive material, and cost more at a given capacity.
CEMA surcharge angle drives belt conveyor capacity: 5 deg for very flat wet-sticky clay up to 30 deg for irregular stringy fibrous material, typically 5–15 deg below the static angle of repose. Use As, not Ar, for cross-section area in Q = A x v x density x 3.6.
ANSI/CEMA 350-2021 material characteristic codes pair a four-part alphanumeric label (e.g., 94A10026M) with a component series (1D, 2D, 3D) to map bulk material abrasiveness, flowability, and density to the correct screw, hanger, and trough build. Codes are selected from the ANSI/CEMA 550-2020 class
Case-coding print resolution directly controls barcode legibility: 300 dpi thermal transfer beats most inkjet for dense narrow-bar codes, while 12 mm character height on corrugated cases requires high-density inks and stable case presentation. Auto print inspection closes the readability loop in rea
Large-character inkjet (LCI) case coders handle porous corrugated, dusty corrugated lines, and rapid SKU changeovers at lower capital cost, while laser case markers deliver permanent, ink-free codes on coated boards, metals, glass, and films at higher resolution but stricter substrate and safety con
Dual-printhead case coders print two opposing sides of a corrugated carton in one pass using a single controller, with two-head TIJ, large-character, and thermal inkjet systems on the market today.
Carton flow shelves drop into existing pallet rack bays on a 3-5% incline, delivering 2-3x the pick velocity of static shelving for case and tote operations. Specify roller vs skate-wheel track, straight vs knuckled shelf, and square-front vs layback frame by SKU size and pick method.
Cantilever racks are the correct pick for long bar stock, pipe, and lumber because their open-front arms eliminate the front uprights that block long loads on selective pallet racks. Selective pallet rack only fits bar stock when the bars are cut, bundled to standard pallet footprints, and handled a
Paper strapping can replace polypropylene (PP) banding for light- to medium-duty bundling of corrugated board, paper, and printed media, but PP retains the edge in UV, moisture, and tension recovery for heavy palletized loads.
Yes, an existing overhead conveyor loop can be extended or rerouted: forged rivetless chain (X348 / X458 / X678), standard I-beam and Unibilt enclosed track sections are modular, allowing on-site additions, curve changes, and re-routing during installation with no full system replacement.
Centrifugal discharge bucket elevators run at 225 to 300 fpm (1.14 to 1.52 m/s) belt speed, with throughput up to 5,000 ft³/h or 150 tons/h on free-flowing granular stock. Speed is set by head-pulley diameter and tip speed needed to throw material clear of the bucket into the discharge chute, not by
Bucket elevator capacity is set by three coupled variables, bucket volume, bucket pitch (spacing), and belt speed, through the equation P = V × ψ × v × 3600. Centrifugal units run wide spacing (projection + 50 mm min, chain pitch 102–305 mm) for up to 15,000 ft³/hr, while continuous-discharge chains
Plastic and steel elevator buckets are not interchangeable: engineering plastics (HDPE, UHMW-PE, nylon, PU) win on weight, corrosion and food-grade hygiene, while carbon/stainless steel wins on abrasion, impact and temperature. Match the bucket to bulk material density, particle size, temperature, m
Head pulley lagging on bucket elevators is selected for friction, not cosmetics: rubber (38-80 Shore A, CoF 0.35-0.45) handles general duty, ceramic tile lagging (CoF over 0.50) suits high-tension drives above 500 PIW, and metal-cored lagging like Metallag addresses hot-product elevators. Drive pull
Blow tank cycle time and batch size are linked by two ratios: the equipment-bound size bottleneck (vessel max fill) and the scheduling bottleneck (longest single-unit operation), and annual throughput = batches per year × batch size. A 10-minute reduction in a 144-minute batch cycle raises a 10-batc
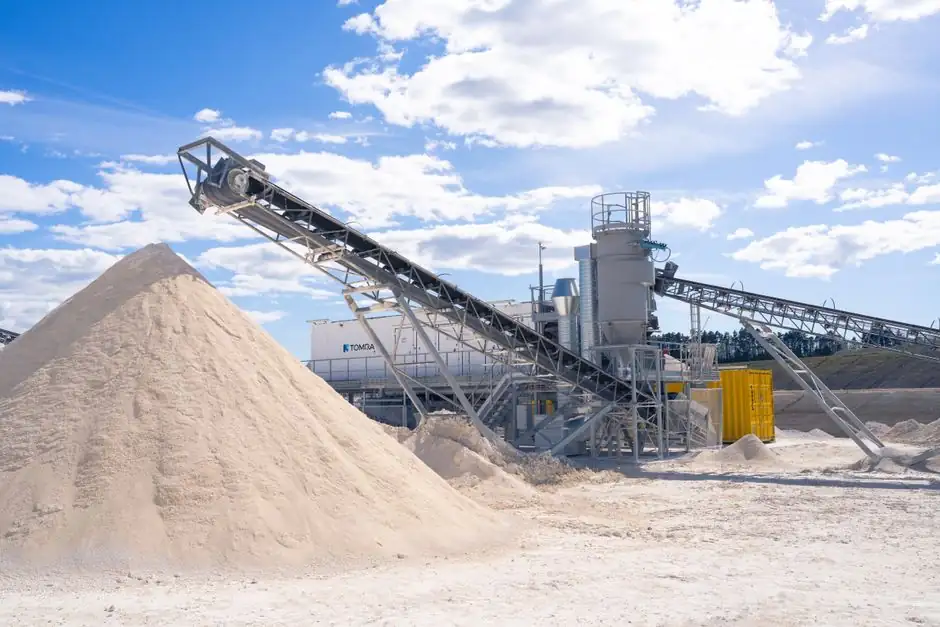
Enclosed screw conveyors (U-trough or tubular) handle enclosed dusty powders at 15-45% trough loading and short 60-80 ft runs; belt conveyors win for long distances and gentle throughput but need covers and dust extraction for dust-tight duty.
Chain-driven bucket elevators outperform belt units on hot, abrasive, or high-shock loads and on tall lifts, while belt units win on cost, noise, corrosion resistance, and capacity up to 5,000 cu ft/h. Choose by material temperature, particle size, lift height, and total cost of ownership.
AMRs built to ANSI/RIA R15.08, ISO 3691-4, and UL 3100 use safety-rated 2D laser scanners sized for ≥270° field-of-view zones and PLd Cat 3 / SIL2 control loops. Typical 2026 platforms pair redundant front+rear scanners for 360° coverage and Class 1M eye-safe emission per IEC 60825-1.
Automatic induction on cross-belt sorters is specified when throughput exceeds roughly 10,000 units per hour and parcel dimensions are consistent; semi-automatic fits 4,000 to 10,000 UPH mixed-SKU operations; manual induction remains viable only below 2,000 UPH. Selection pivots on rate, SKU variabi
Teardrop pallet rack beams are largely cross-compatible between manufacturers that share the universal 2-inch teardrop hole pattern, but mixing brands in the same beam level can warp the frame, and old-style round-pin beams will not drop into new-style teardrop uprights. New-style teardrop beams fit
Hand pallet truck, pump truck, and manual pallet jack are three regional labels for the same human-powered hydraulic pallet-moving tool. Capacity typically spans 2,000 to 6,600 lb, lift height stays at 190-200 mm, and the device is entirely distinct from electric-powered pallet movers that use motor
ANSI/A3 R15.08-1-2020 (reaffirmed 2026) is the North American safety baseline for industrial mobile robots, splitting risk reduction across three parts covering the robot, site integration, and end-user duties.
ANSI/ITSDF B56.5-2024 is the current U.S. safety standard for driverless AGVs and the automated functions of manned industrial trucks, replacing B56.5-2019 and governing design, hazard-zone speeds, object detection, and e-stops. ISO 3691-4 covers the same scope internationally, and UL 3100 addresses
Set the applicator tamp-pad angle between 20° and 45° to the conveyor surface, match conveyor height to a median product height, and lock the head before running line trials. Re-check angle whenever label length or substrate stiffness changes.
AGVs follow fixed paths defined by wires, magnetic tape, or laser reflectors, while AMRs use onboard LiDAR and SLAM to plan routes dynamically and reroute around obstacles. For stable, heavy, high-precision work, AGVs remain the better fit; for fluid, high-variability workflows, AMRs deliver the fle
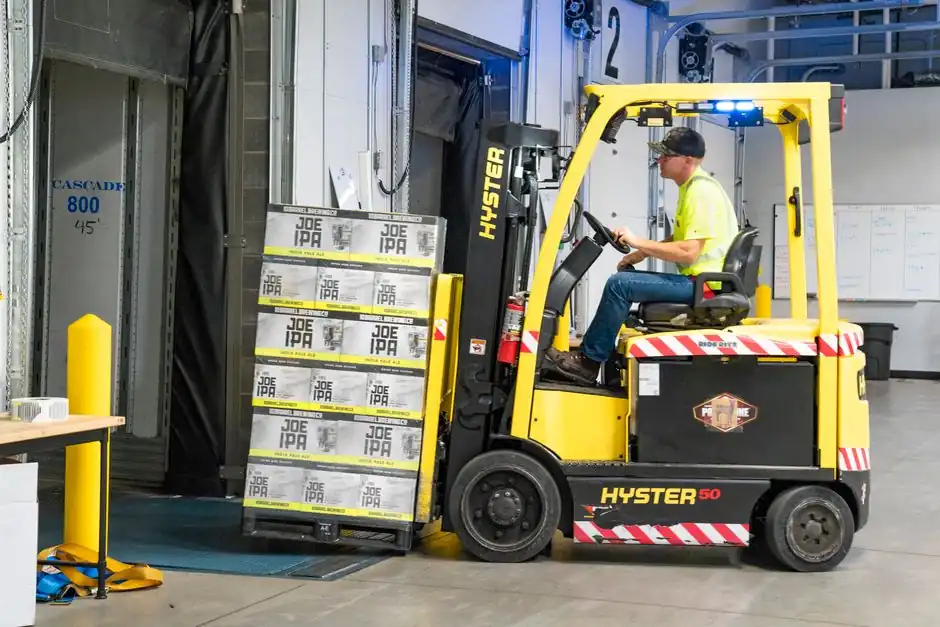
Underride (cart-lift) AGVs slide beneath trolleys and raise them via a lifting mechanism, while conveyor-top AGVs carry the load on an integrated deck or belt on top of the vehicle. Underride units are simpler, cheaper, and fit automotive line-side cart trains; conveyor-top variants handle palletise
AGV guidance is a four-way tradeoff between accuracy, infrastructure cost, layout flexibility, and maintenance load: wire/magnetic tape gives fixed-path reliability, laser triangulation with reflectors delivers ±5–10 mm accuracy, vision-based guidance avoids floor installation, and natural-feature S
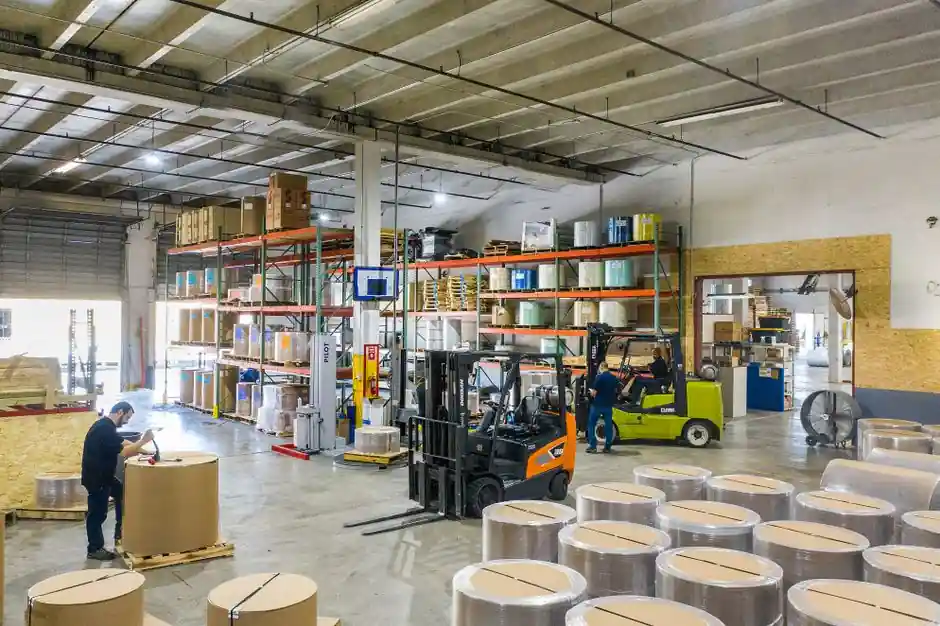
Unit-load AGVs handle single pallet transport via fork or under-ride lift, while tow tractors pull trains of carts at higher throughput over longer distances. Match payload per trip, aisle width, and floor-load rating to pick the right family.
Opportunity charging wins for most 24/7 AGV fleets because it tops up lithium packs in short, frequent windows without taking vehicles offline, while battery swap stations trade that simplicity for higher throughput and lower per-station infrastructure cost in large, heavy-payload operations.
For shift-length AGV operation, size the pack to required energy (Wh) = average power (W) × shift hours, then add a 20–30% margin for depth-of-discharge, end-of-life loss, and auxiliaries. A 2,000 W load over 8 h becomes 16,000 Wh base and ~20 kWh nominal; LFP chemistry with opportunity charging is
AGV safety laser scanners for obstacle detection typically offer 190–300° field of view, 3–9 m protective field range, and PLd/SIL2 rating per EN ISO 13849 and IEC 62061. Operating range is set by speed, response time, and braking distance, not maximum range alone.
An AGV drive unit combines an onboard motion controller with a traction motor, planetary gearhead, and drive wheel into a single flange-mounted assembly, most commonly built around a brushless servo or hub gear motor. The dominant traction technologies are brushless DC, brush DC, stepper, and AC syn
AA, CC, and low-profile elevator buckets solve three different problems: AA is the high-capacity industrial centrifugal workhorse in ductile iron or aluminum, CC trades some capacity for closer belt spacing and gentler discharge, and low-profile variants of either family cut back height to pack more
Shrink wrapping machine sizing is a physical-fit decision driven by product envelope, sealing architecture, and tunnel aperture, not by catalog blade length. Match chamber, semi-automatic L-bar, or fully automatic lines to SKU mix, daily volume, and film type (POF, PVC, PE) before approving a config
For food and beverage lines, the strongest shrink wrapping picks in 2026 are automatic L-bar sealers running 30-40 packages/min for retail packs, automatic sleeve or bundling sealers with polyolefin (presentation) or polyethylene (transit) film for multipacks, and semi-automatic units for small oper
Pick a shrink wrapping machine by matching three specs to your line: product size envelope (L x W x H), daily volume bracket (under 100, 100-500, 500+, or 10,000+ packs/day), and film type (LDPE, POF, or PVC). Match those against manual, semi-auto, or full-auto architectures, then verify tunnel leng
Case packing machine suppliers split into OEM builders (Combi, Massman, Hamrick, Pearson, Brenton), refurbishers, and distributor-dealers (Crown Packaging, Massman Automation, DMM Packaging). Pick by load style (top, bottom, end/side, wraparound), speed class, and footprint rather than brand alone.
Case packer selection hinges on four anchors: product type, case style, throughput, and line integration. Top-load, side-load, and wrap-around each fit a different duty; speeds typically span 10 to 120 cases per minute by configuration.
For pharmaceutical lines, a top-load or wrap-around case packer from IMA, Marchesini, Syntegon, Serpa, or Combi typically delivers the required GMP hygiene, format flexibility, and 4-50+ cases/min throughput. Selection hinges on product geometry, dust containment, changeover time, and validation doc
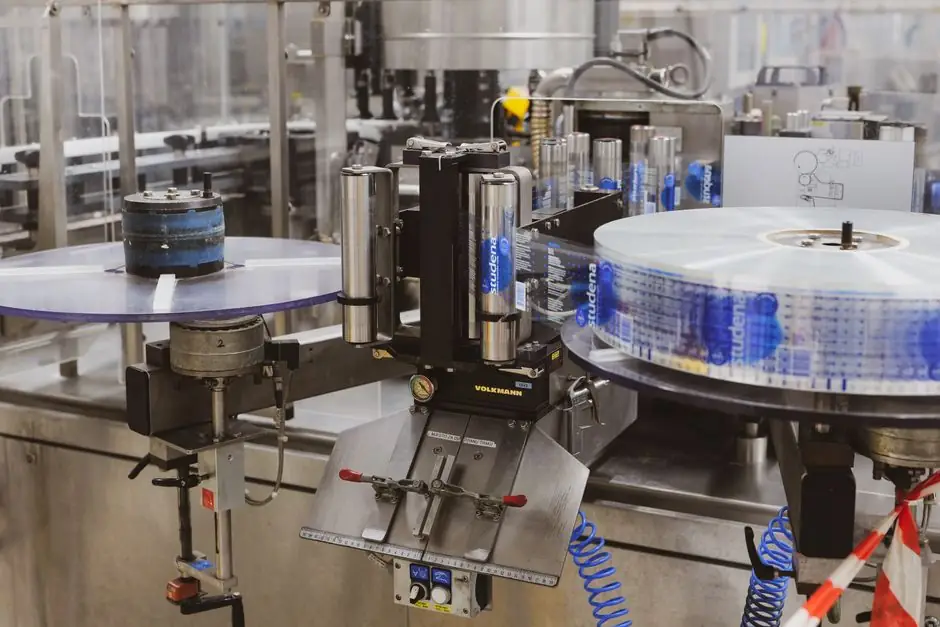
Choose a case packing machine by matching four decisions to your SKU mix: top-load, side-load, bottom-load, or wraparound architecture; mechanical vs. robotic load; throughput in cases per minute; and the case-blank style (RSC, knock-down, tray, or wraparound). For SKU-stable lines above roughly 30
The global labeling machinery market generates roughly $15 billion annually, with suppliers split between high-speed OEM integrators (Krones, Sidel, KHS, Herma, Accraply) and regional builders (CTM, Universal Labeling, Accutek, Auto Labe, Primera) serving bottles, pails, and warehouse print-and-appl
Automatic labeling machine selection is driven by four decision axes: container geometry (round, flat, square, irregular), label substrate (pressure-sensitive, shrink-sleeve, glue-applied), throughput band (semi-auto under 30 BPM vs auto 60-400 BPM), and line-integration duty. Match machine type to
For water treatment plants bottling purified or mineral water, an automatic wrap-around labeling machine running 100-350 bottles per minute is the default choice, with servo-driven tech and stainless-steel contact parts for hygienic lines.

Choosing a labeling machine comes down to four engineering decisions: container geometry (round, flat, square, irregular), throughput band (manual tabletop under 30 cpm, linear 30-150 cpm, rotary 150-600+ cpm), label technology (self-adhesive, hot-melt glue, sleeve-shrink, wet glue), and the post-la
Sizing a capping and sealing machine starts with the closure type and torque window, then matches throughput in bottles per minute to container diameter, cap material, and CIP/SIP hygiene class. Pick spindle or chuck for screw caps under 60 BPM, ROPP for tamper-evident aluminum over 100 BPM, and sna
For oil and gas packaging, the best capping and sealing machine pairs induction cap sealing with servo torque-controlled chuck cappers, matching cap diameter, viscosity, and line speed. Options from Enercon, Tedelta, and VKPAK cover 6000 bph high-speed lines down to manual bench units, with PET, gla
Pick a capping machine by matching cap type, container geometry, and torque accuracy to your throughput, not by chasing the fastest head. Spindle and chuck cappers cover most screw-cap lines, ROPP and chuck cappers suit threaded security closures, and snap or press-on cappers are correct for unthrea
North American filling machine suppliers listed on independent B2B directories now offer nine core filling technologies, from piston and overflow liquid fillers to auger, VFFS and aseptic pharmaceutical lines. Buyers shortlist by container, viscosity and cGMP class, then validate via lab testing and
For e-commerce fulfillment, filling scale selection should be driven by order profile (single-unit, multi-unit, kitted), SKU weight band, and target throughput. A bench/checkweigher is the common anchor at the pack line; a filling machine-integrated weigh/fill station suits kitted or bulk-SKU flows
Filling machine selection hinges on matching viscosity, container, and throughput: piston or pump fillers handle viscous products, gravity or overflow suits thin liquids, and auger/cup fillers cover powders and granules. Accuracy runs ±0.2% to ±2%, with manual units under 900 containers per hour and
For e-commerce fulfillment, pick a dynamic checkweigher that matches peak packages-per-minute, has a capacity range spanning the lightest and heaviest SKU, supports OPC-UA/MQTT to the WMS, and uses reject devices sized for fragile parcels. US automatic-checkweigher demand reached USD 102.3 million i
For retail distribution, FIBC bulk bags in the 1,000-2,000 lb range with 5:1 or 6:1 safety factors and Type C/D static control are the practical spec envelope, chosen by bulk density, particle size, and lift equipment rather than price alone.
Wrapping machine selection for e-commerce fulfillment hinges on matching four machine families, case erectors/sealers, shrink wrappers, banding/strapping, and pallet stretch wrappers, to SKU mix, throughput, and right-sizing goals. Automation typically lifts packaging throughput 30–50% versus manual
Coding and marking hardware for warehouse automation is selected by substrate (cardboard, plastic, PE, metal), line speed, and DPI rather than brand: TIJ for low-duty case coding, CIJ for high-speed non-contact lines, laser for permanent marks, and print-and-apply for pallet labeling. ROI is typical
For apparel distribution checkweighers, target ±1-2 g accuracy at 100-300 ppm on polybagged sets, EMFR load cells for premium labels, strain gauge for cost-driven lines, and verify ISO 9001, GMP, and OIML R76 compliance before purchase.
Electronics handling demands ESD-safe, gentle, and traceable sortation, with divert-and-transfer roller sorters (35-50 parcels/min) fitting small-package lines and dedicated PCBA recovery systems targeting the 3-5% annual e-waste growth. Choose by part size, sensitivity, and traceability needs.
For apparel distribution, the dominant sorter choice is a tilt-tray or pocket sorter with WMS-driven routing, specified at 2,000+ parcels/hour, 20+ destinations, and mixed soft polybag/carton/return handling. Cross-belt wins on speed for uniform parcels; push-tray and put-walls serve smaller operati
For chemical shipping, divert-and-transfer roller belt sorters and sliding-shoe sorters dominate because they handle sealed chemical pouches, polybags, and 1-25 kg cartons without the gaps that catch flexibles. Specify by parcel weight, throughput (35-50 ppm typical for divert-roller, 60-120 ppm for

Electronics handling docks should specify a 6 ft wide pit-installed hydraulic leveler, 25,000-80,000 lb capacity, sized 25-30% above the heaviest forklift-plus-load, with a 16 in lip and ANSI MH30.1 compliance. Edge-of-dock units fit only low-volume, light-duty bays.
Cold chain AGV selection hinges on three spec gates: rated operating temperature (commonly -25°C, with controllers qualified to -30°C), navigation tolerance for ice fog and condensation on lidar, and battery chemistry that holds capacity at sub-zero duty. Choose an AGV with stainless structural opti
Semi-automated pallet shuttle systems are the practical default for electronics handling SKUs with high pallet-per-SKU counts, deep-lane storage to 60+ m, and -30°C cold-store compatibility. Full ASRS only pays back at hundreds of pallet moves/day, so shuttle racking wins for mid-throughput SMT, com
Apparel distribution centers select shuttle systems by SKU velocity, ceiling height, and channel depth: 2-way shuttles suit high-throughput FIFO pallet flows, 4-way shuttles fit low-clearance sites, and box-level shuttle AS/RS serves hanging-folded item picking. Pallet shuttle is the wrong tool for
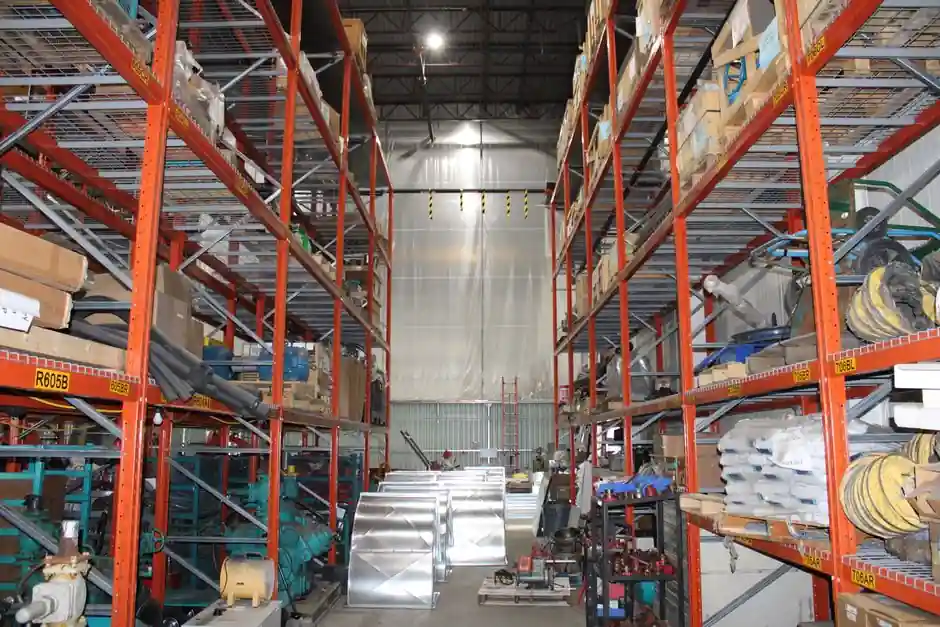
Retail distribution centers choose between two-way and four-way pallet shuttle systems: two-way for deep-lane, single-direction buffer storage on a budget; four-way for cross-aisle flexibility and multi-level retrieval. Match the shuttle to SKU count, throughput target, ceiling height, and floor loa
For apparel distribution, AGV robots work best on fixed-path, high-volume carton and pallet runs between receiving, sortation, and outbound, where a single garment style can spawn 10-20 size/color SKUs. For SKU-dense each-picking of soft goods, AMR mobile robots with specialized soft-gripper cells a
AGV robot selection for warehouse automation hinges on payload, path stability, and integration depth: magnetic-tape AGVs suit repetitive full-pallet moves, while SLAM-based AMRs cover dynamic tote workflows. Typical 2026 AGV fleets target 1,000–3,000 kg payloads with laser or QR navigation.
For chemical shipping, AGV selection hinges on four axes: payload class (300–5,000 kg), navigation method (track-guided vs natural feature), ingress protection plus hygienic/ATEX-rated chassis, and zone-based safety scanners. Stainless-steel VARIO MOVE units operate between –40 and –40 degrees, whil
AGV selection for automotive parts logistics hinges on payload, navigation method, and route stability: magnetic-tape/laser-guided AGVs fit fixed, high-volume lineside runs, while SLAM-based AMRs suit mixed-model changeovers. VisionNav's VNP15 pallet stacker and Pudu Robotics' 2026 guidance anchor c
Pallet shuttle systems in chemical warehouses use motorized carriers to move pallets inside deep-lane racks, raising storage density over drive-in racking and supporting FIFO rotation for expiry-sensitive goods.
Pharmaceutical distribution centers selecting stacker cranes should prioritize unit-load class, temperature rating, and WMS/WCS integration; single-mast cranes suit pallet loads up to 1.65 t to 148 ft, while double-mast designs handle heavier SKUs in cold-chain and 3PL hubs. The global market reache
For e-commerce fulfillment, AGV selection hinges on payload class, navigation type, and goods-to-person fit: magnetic-stripe AGVs suit fixed routes and 24/7 pallet loops, while laser SLAM AMRs handle dynamic piece-picking aisles at typically 60–80% labor overhead reduction.
Stacker cranes for retail distribution typically run as unit-load AS/RS systems reaching 40 m (131 ft) in aisles as narrow as 1.5 m (5 ft), cutting footprint versus block stacking by up to 40%. Selection pivots on mast configuration, load weight, and throughput, with global market value at USD 1.27
Pneumatic conveying systems move dry bulk cargo through sealed pipelines using positive pressure or vacuum airflow, split into dilute-phase (high velocity, low pressure) and dense-phase (low velocity, high pressure) families. For air-cargo handling of seed, feed, plastic pellets, and powder, dilute-
Vibrating conveyors are specified for cold chain logistics when bulk product is fragile, sticky, or frost-prone at 0 to 10 °C chilled and -30 to 0 °C frozen zones, and they outperform belt, screw, and drag units on jam risk, energy draw, and maintenance burden.
For apparel distribution, unit-load pallet stacker cranes with single-deep FIFO layouts dominate, while double-deep and unit-mast mini-load cranes cover overflow and hanging-garment picking; sizing hinges on SKU count, ceiling height, and carton vs. hanging SKU mix, with global market value projecte
Vibrating conveyors are bulk-material machines built for powders, granules, and parts, not soft, irregular apparel. Apparel distribution centers needing horizontal garment, polybag, or carton flow should evaluate chain, roller, and pneumatic systems first. Vibratory units still have a narrow role: h
Vibrating conveyors for pharmaceutical distribution are specified as natural-frequency or electromagnetic units with stainless contact surfaces, low-amplitude high-frequency motion, and contained troughs suited to tablet and powder transfer. Selection hinges on throughput, containment class, cleanin
For retail distribution, pneumatic conveying works best as a sealed, dust-controlled transfer between silo, bulk bag, and packaging line, with dilute phase for free-flowing granules and dense phase for friable or cohesive products. Selection is governed by particle size, moisture, friability, abrasi
Port-logistics pneumatic conveying is selected by matching material physics, phase (dilute vs dense), pressure or vacuum mode, and pipe routing against ship-unloader throughput, dust-control and ATEX/IECEx zoning. Most port cement, fly-ash and grain terminals standardize on dense-phase or semi-dense
Pneumatic conveying selection for pharmaceutical distribution hinges on matching dense-phase or dilute-phase, pressure or vacuum mode to API/excipient fragility, containment class, and GMP cleanability. Coperion P-Series and Gericke dense-phase lines target tablet granulations, while rotary valves a
Pneumatic conveying moves dry bulk food ingredients through enclosed pipelines using positive or negative air pressure, and the four main types (dilute phase pressure, dense phase pressure, vacuum, and combined) are matched to powder properties like bulk density, particle size, and friability. Selec
Pharmaceutical-grade bucket elevators for powders and granules prioritize sanitary construction, FDA-approved contact materials, CIP capability, and gentle handling, with centrifugal, continuous, and positive-discharge types selected to match material flow behavior.
Chain conveyors win in warehouse automation when loads exceed roller limits, but the right pick hinges on weight, traction, and AMR integration. Engineer-grade decision map and 2026 benchmarks below.
Chain conveyors for air cargo terminals are specified for horizontal in-house pallet (IHP) transfer inside ASRS, with 1,300 kg per position, 1,750 mm standard length, and -30°C to +60°C operation. Selection pivots on unit load vs. bulk commodity, throughput envelope, and ASRS integration.
For automotive parts logistics handling plastic pellets, metal chips, and stamping scrap, dilute-phase positive-pressure pneumatic conveying at 15-30 m/s air velocity is the default 2026 spec, with dense-phase reserved for abrasive or friable parts. Selection hinges on material bulk density, particl
Warehouse automation projects sized under 1,000 kg/hr typically pair dilute-phase vacuum pneumatic conveying with rotary valve feeders and ceramic-backed elbows, while dense-phase positive-pressure systems win for abrasive, friable, or hygroscopic bulk solids above 10 t/hr. The right pick comes down
Dilute-phase vacuum pneumatic conveying is the standard pick for apparel distribution centers moving garments, hangers, and trim, due to short runs, low abrasive load, and tight dust control. Dense-phase or pressurized systems are ruled out for most apparel moves because of fiber damage and overcapa
Pneumatic conveying for electronics handling is specified as vacuum dilute-phase in 80% of cleanroom-adjacent SMT feeder and tray-loader applications, with dense-phase limited to abrasive or friable oxide and solder powders. Selection is governed by material bulk density, particle size distribution,
Pneumatic conveying selection for chemical shipping hinges on three coupled choices: dilute-phase (700–1,000 m/min, mass ratio under 15) versus dense-phase (around 200 m/min, ratio 100+), pressure versus vacuum, and air versus inert gas, all driven by material properties, distance, and safety class.
Sorting systems classify into three product-load tiers (unit, box/container, pallet) and several morphology variants (tray, shoe, vertical, cross-belt), with 90-degree units rated 10-60 cartons/min. Selection is driven by item size, fragility, throughput, and destination count rather than a single s
Bench scales are compact tabletop weighing instruments covering roughly 2.5 to 500 kg capacity at high readability, ideal for laboratory, retail, and light industrial use where accuracy and footprint matter more than raw capacity. Their main trade-offs are limited platform size, sensitivity to overl
Mesh belt conveyors offer high-temperature tolerance up to 260°C, open-mesh airflow, and easy wash-down, but trade off on price, abrasion resistance, and load capacity versus modular plastic or fabric belts. Specify PTFE mesh for hygienic, hot, or corrosive lines; choose balanced weave or ladder-fle
Sorting system installation hinges on five concrete checkpoints: ground flatness ≤2–3 mm/m, track butt joint gap ≤0.5 mm, grounding resistance ≤4 Ω, CE/EN 12100 compliance, and a 72-hour re-leveling audit after commissioning.
Shuttle systems in intralogistics split into four structural classes: level-bound, multi-level, pallet (1D/2D/3D), and free-roaming AGV/AMR hybrids. Each class trades aisle footprint, throughput (60 to 1,000+ double cycles/aisle), and load carrier (boxes, totes, pallets) for specific build heights a
Overhead conveyors are mechanical transport systems suspended above the production floor, classified by drive type (powered, free, power-and-free), track profile (enclosed track, open I-beam, C-section), installation orientation, and load class from roughly 1 lb to 10,000 kg.
A checkweigher installation has three failure-prone stages: site preparation, mechanical mounting of the weigh station, and electrical commissioning of the controller. Spec the platform as a stand-alone conveyor island, run 110 VAC or 24 VDC I/O via the documented card options, and complete both sta
Checkweighers split into static (benchtop, lower cost, manual QC) and in-motion (conveyor, 100% inspection, dynamic weighing) classes, with washdown, combination, multi-lane, and pharmaceutical variants as specialized sub-types.
Carton erecting machines deliver 20-50 cases/min throughput, cut manual forming labor, and hold carton squareness within tight tolerances, but they demand specific blank hardness, carry a 3-10x higher upfront cost than manual stations, and constrain SKU flexibility. They pay back when daily volume c
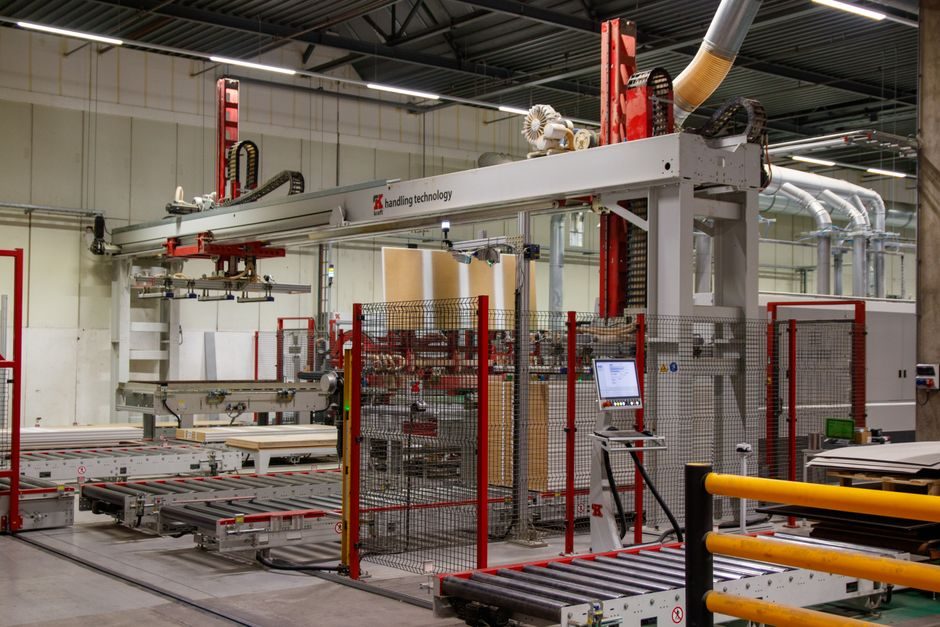
Overhead conveyor line costs in 2026 typically span USD 80-600 per metre for light-duty X-348/X-458 chain, with engineered paint-line and food-grade systems running USD 1,500-6,000 per metre installed, driven by chain spec, corrosion package and drive-station sizing.

Capping and sealing machines split into four drive families — spindle, chuck, side-wrap, and induction — with throughput ranging from 30 BPM benchtop units to 200+ BPM rotary cappers. Selection is driven by cap type, container geometry, line speed, and hygiene class rather than brand. This reference
Overhead conveyor selection for retail distribution centers pivots on three specs: unit load (lb/kg per carrier), part spacing (chain pitch in inches), and total drive pull (lb). Cable conveyors hold ~19% of the global overhead conveyor market and are common in retail DCs, garment plants, and baggag

Screw conveyors for air cargo ground handling are uncommon; only specific duty cases — de-icing fluid recovery, ULD ballast sand reclamation, and bulk in-flight catering loading — warrant consideration, with inclined 30° tubular units in 304/316 stainless steel being the practical default. Operators

Stretch wrapping machines stabilize pallet loads with 17–23 µm LLDPE film, while vacuum packaging machines evacuate chamber air to ≤1% residual O₂ for shelf-life extension; choice hinges on whether the goal is load containment or product preservation.
PP and PET strapping bands and corrugated carton boxes are complementary, not interchangeable, packaging elements. Spec the band for tensile load and elongation, spec the carton for ECT/BCT stacking strength, and match the duty cycle to your strapping machine class.

Overhead conveyors are well-suited for chemical shipping when loads are irregular, hanging, or routed through hazardous zones where floor conveyors cannot safely travel, per IQS Directory and Richards-Wilcox Conveyor guidance. Selection must be driven by payload weight, corrosion class, track enclos
Strapping band selection in a 2026 warehouse-automation context pivots on three decisions: PET for heavy palletized loads, PP for light carton runs on automatic strapping machines, and steel only where heat or sharp edges rule out plastic. Match band material to machine class, not the other way arou

Screw conveyors for port bulk handling are typically specified as horizontal or inclined units up to 30°, with elevations to 45° achievable through proper design; shaftless or heavy-duty shafted units dominate ship-loading and stockyard duties. Selection hinges on material characteristics, inclinati

Industrial coding machines deliver non-contact, high-speed marking across metal, glass and plastic at 30-600+ characters per second, but ink viscosity limits, substrate porosity, and per-character ink costs constrain where they outperform labeling machine and cutting machine alternatives. Selection
Wire mesh storage cages and HDPE plastic pallet boxes serve overlapping but distinct warehouse roles; the 2026 spec range for rigid plastic boxes spans 202 L to 1,400 L (Carttec R90468 to Cabka Pallet Box 2.0 6R), while collapsible wire cages sit in the 50-piece MOQ tier at roughly US$80 FOB Ningbo.
VLM selection for pharmaceutical distribution hinges on three spec gates: closed-tray containment for dust and cross-contamination control, dual-level delivery with WMS/ERP integration, and validated cleanroom-class construction. Europe holds 37% of 2024 VLM demand, and the global market is forecast

Roller conveyors split into gravity, motorized/chain-driven and belt-driven classes covering 90 kg/m light-duty to 4,500 kg pallet handling, with roller Ø48-89 mm steel, PVC or stainless tubes on frames from 0.5 m telescopic to 12.5 m extendable straight runs.
For cold chain logistics, specify a conveyor sorting line on stainless frame with PU/food-grade belt, IP65 controls, and ±0.1 kg inline checkweighing to keep throughput above 2,000 parcels/hour at -25°C dock zones.
Choosing a wrapping machine starts with matching the geometry: radial or axial reel wrappers for coils and paper rolls, ring-type eye-through wrappers for steel coils, pallet stretch wrappers for palletised loads, and high-speed profile wrappers for aluminium extrusions. Confirm PLC control, film te
Conventional pallet rack and AS/RS serve different storage-density and throughput tiers, with selective pallet rack running roughly 25-40% of the per-pallet-position capital of unit-load AS/RS, while AS/RS systems routinely reach 20-30 m heights versus 8-12 m for standard racking.
Bench scale total cost of ownership is dominated by 5-10 year lifecycle costs—calibration, validation, downtime, and data integrity—not the unit price. A TCO model for bench scale buyers should price acquisition at 20-40% of 10-year spend, weigh IP65/IP69K vs IP43 stainless choices, and lock the cal

Checkweigher TCO spans purchase, operation, training, maintenance, and disposal over a typical 10-15 year service life. The biggest cost drivers are calibration drift, reject-device wear, and CIP washdown corrosion, not the headline unit price.

Plastic turnover boxes — defined as reusable, stackable industrial containers covered under the broader turnover box family — trade material toughness against cold performance and cost. HDPE units offer high impact strength for heavy loads but deform under sustained load and lose toughness in cold;
Mesh belt conveyor selection for apparel distribution: spiral-grid or flat-flex stainless mesh with 2.5-6.0 mm wire diameter, 6-12 m/min speed, food-grade AISI 304 grade suits garment carton and polybag lines without contamination or marking.

A chain conveyor is specified for heavy, abrasive, hot, or high-torque bulk-handling duties that exceed a belt conveyor's grip and temperature envelope; selection hinges on chain class, pitch, pin/wheel material and the matching roller chain or drag geometry, not on frame width.
For pharmaceutical distribution, a manual pallet jack in 304/316 stainless steel with a 2,000–3,000 kg capacity, hygienic sealed hydraulics, and FDA-grade nitrile seals is the baseline spec, with electric washdown models reserved for high-throughput DC operations.
AS/RS systems raise storage density, cut labor, and improve inventory accuracy inside warehouses and distribution centers, but they impose high upfront cost, rigid throughput limits, and heavy dependence on specialized maintenance. Specify an AS/RS system only when SKU velocity, ceiling height, and
Shuttle systems for port logistics are specified around three hard gates: corrosion resistance (ISO 12944 C4/C5), dynamic load securing under deck vibration, and crane/shuttle interface throughput. Bistable electromagnetic load-securing solenoids (e.g. Kendrion BSM family) eliminate continuous holdi
Belt conveyor selection for warehouse automation hinges on payload class, belt type, drive layout, and sanitation rating. Pharmaceutical and food facilities typically specify food-grade flat belt materials and 30 cpm rated case flipper units.
Overhead conveyors in cold-chain logistics require a power-and-free or enclosed-track chain conveyor with stainless or galvanized carriers, low-temperature lubricants rated below -25°C, and a drive sized for the heavier garments of insulated garments and packaging. Stainless steel racking and refrig
Manual pallet jack TCO is dominated by 5-10 year cost lines beyond purchase price: operator injury, load-handling cycle time, hydraulic seal rebuilds, steer-wheel and load-wheel wear, and battery-free simplicity. A 5,500 lb unit purchased at $300-$700 typically accrues 2x-4x its purchase price in do

Bucket elevators move bulk material vertically up to 200 m using spaced buckets on a belt or chain, while belt conveyors carry continuous loads horizontally or on shallow inclines. Choose a bucket elevator for vertical lift of free-flowing dry bulk, and a belt conveyor for horizontal run, mixed part
2026 case packer pricing runs roughly USD 25,000 for semi-automatic top-load units to over USD 350,000 for multi-axis robotic top-load/tuck-in lines, with total cost of ownership driven by format flexibility, guarding and integration, and ongoing spares. This guide benchmarks specs, options, and sou
Autonomous Mobile Robot (AMR) selection for warehouses hinges on four 2026 spec gates: payload class (50–1,500 kg), navigation stack (SLAM on ROS vs. line/QR-following AGV), WMS/ERP interface, and floor-condition tolerance. Match duty cycle, aisle width, and picking model before vendor demos.

Chinese dust collector system manufacturers dominate the global B2B supply map in 2026, with named suppliers offering baghouse, cyclone, and wet scrubber units from US$700 to US$52,000 across metallurgy, foundry, woodworking, and asphalt applications. Specifiers should match filter media, airflow cl
An FIBC bulk bag's true landed cost runs roughly 1.6× to 2.4× its ex-works price once you fold in liner loss, fill-and-discharge labour, and one-trip vs multi-trip SWL decisions; PP fabric, UV rating, and antistatic certification move the price more than bag geometry does.

Chain conveyors for e-commerce fulfillment are specified by tote size, sortation throughput, and WMS/EDI integration rather than raw chain pull. For 2026 builds, dual-strand drop-forged chain on accumulating roller beds, paired with HMI/WMS real-time sync, is the baseline pattern at 3PL hubs handlin

Pallet stretch wrapper pricing spans roughly USD 2,500 for entry-level turntables to USD 18,000+ for robotic cells, with the cost driver being turntable diameter, pre-stretch ratio, and PLC integration. The biggest landed-cost swings are duty, film gauge, and warranty length, not the machine's FOB p
Pick a pallet stacker for ground-to-low-level pallet moves (≤6 m, single-pallet loads, 1.0–2.0 t) and an order picker for case-level picking above 3 m (typically 4.5–12 m, multi-line SKUs). Mixing them is the most common spec error in 2026 small-warehouse sourcing.
Vertical Lift Module (VLM) installation is a six-stage site-to-commission workflow covering floor load, ceiling clearance, tray payload, and WMS hookup, with units like Modula Lift reaching 120 trays/hour and 990 kg per tray. The global VLM market is projected to grow from US$950.19 million in 2024

Belt conveyors for chemical shipping are typically specified with stainless or ceramic idlers, chemical-rated belt covers, and corrosion-resistant pulleys. Selection hinges on chemical compatibility, belt width 500-1400 mm, trough angle 20-45°, and centre distance up to 20 m per drive.

Installing a filling scale requires a clean rigid base, level verification to within 0.5 mm/m, calibration with F-class or better test masses between 1 g and 50 kg, and a 24 V DC supply with shielded cable for load-cell integrity. Acceptance is typically a repeatability deviation under 0.1% of full

As of June 2026, 12 manufacturers list 20 automatic-storage stacker-crane systems and 50 ASRS stacker-crane units on DirectIndustry, with Vanderlande, System Logistics and Automha leading the European tier and EBILTECH, Changsha Kenwei and Henan/Luoyang suppliers dominating the China price tier from

Strapping band installation in 2026 hinges on matching PP or PET band width, thickness, and break-strength to the load, the strapping machine class, and the seal type. PP at 9-19 mm and 0.5-1.0 mm with 60-380 kg break-strength covers most pallet work, while PET 12-19 mm at 0.6-1.2 mm handles 200-600
Storage cage selection for e-commerce fulfillment hinges on three criteria: SKU velocity zoning, mesh aperture matching the smallest carton face, and stackable footprint that survives parcel carrier handline. Match shelving to ABC velocity, pick carton flow rack for fast movers, and use heavy-duty s
Vibrating fork level switches detect point level in liquids and bulk solids at -196 to +450 °C and up to 160 bar, while dock levelers bridge trailers and loading bays at 20,000-80,000 lb capacity. They solve opposite problems and rarely overlap.
Electronics-handling belt conveyors are flat or modular PU/PVC belts on low-noise drum drives, selected on ESD-safe surface resistivity, 5-30 m/min speed, ≤60 kg/m load, and FDA/EU-grade contact materials. They are NOT a fit for heavy ore, scrap, or 1,100 t/h quarry tonnage. Match belt type, idler,
Filling machines are classified by metering principle (volumetric, gravimetric/loadcell, flowmeter, vacuum, piston, auger) and by automation level, with SS 304/SS 316 contact parts and PLC control now baseline for food, beverage, pharma, and chemical lines. Choice hinges on product viscosity, foamin

For pulp and paper plants, the best filling machine is not one single SKU but a 3-stage build: a net-weight or flow-meter filling machine for liquid chemicals and starch, a servo-driven auger filler for titanium dioxide and clay powders, and a 20–1500 L robotic pallet drum/IBC line for slurries — al
Sorting-system selection for warehouse automation hinges on matching throughput, SKU profile, and footprint to four dominant architectures: cross-belt, tilt-tray, sliding-shoe, and put-wall/robot. Cross-belt and tilt-tray suit 5,000–20,000 items/hr parcel hubs; sliding-shoe fits apparel and polybag
Apparel distribution conveyor sorting lines are best specified as garment-on-hanger (GOH) systems with pressure-free accumulation, since hanging goods tolerate zero compression between units. For carton-heavy apparel DCs, cross-belt sorters dominate, while trolleyless overhead pin/latch conveyors se
For electronics handling and storage, a wire-mesh security cage with welded panels, 10-gauge mesh, and roof panels is the practical choice; a true Faraday-cage ESD enclosure is a separate, conductive-material requirement for static-sensitive components outside an EPA.
Storage cage selection in automated warehouses hinges on rack tolerances within 1/8 inch for AGV/AMR compatibility, modular wire-mesh panel widths of 1-10 ft, and stacker-crane friendly clearances. Match cage construction to automation tier before specifying.
For automotive parts logistics, welded steel storage cages with 2,000 kg load ratings and foldable stack-4-high designs remain the default, while HDPE/PU-profile custom racks now lead zero-defect line-side delivery. Match cage type to part fragility, return-loop density, and AGV/JIT compatibility.
Food and beverage storage cage selection hinges on material grade (NSF chrome wire, 304/316 stainless), mesh opening size, load class, and wash-down rating. Wire mesh, dunnage, and security cages dominate, sized in inches and rated by NSF or epoxy-coated carbon steel.
Cold-chain storage cages must be selected for stainless or hot-dip-galvanized construction, food-grade floors, and pallet-compatible footprints to survive -25°C condensate cycles and HACCP audits; mobile racking can lift cold-storage capacity by up to 90% versus fixed layouts.
For apparel distribution, specify food-grade HDPE caged composite IBCs in 275 or 330 gallon capacities with UN/DOT certification; 304 stainless steel is justified only for hot dye or high-purity detergent streams above 60 °C.
For e-commerce fulfillment, HDPE composite IBCs in 275-330 gallon (1,040-1,250 L) sizes dominate pick-pack operations, with 4-way fork entry, 2-inch NPT discharge valves, and UN/DOT-certified composite designs the spec pattern that actually clears a busy DC floor.
Port-side storage cages are welded or collapsible steel mesh containers, typically Q235 grade, in ISO pallet footprints of 1200x800 mm or 1200x1000 mm, with 1000-1500 kg payloads. Mesh-side, solid-side, and timber-base variants dominate 2026 procurement, with fold-flat returns cutting drayage costs
Apparel distribution favors Type A or B woven polypropylene FIBC bulk bags in the 2,000-3,000 lb range, sized roughly 35x35x50 in with 4-loop cross-corner lifts, 5:1 SF, food-grade liners optional.
IBC totes sized 275-330 gallons (1040-1250 L) on a 45"x45" base dominate port liquid logistics by replacing up to 24 drums per 4 units, with HDPE, stainless 304/316L, and carbon steel bodies selected by cargo chemistry, while UN/DOT 31HA1/Y rating and 30-month retest cycles govern dangerous goods ha
Selecting an FIBC bulk bag for chemical shipping hinges on matching UN hazard class and Type A/B/C/D static control to the product, with 5:1 or 6:1 safety factors and UN drop/stack testing mandatory for hazardous goods.
For automotive parts logistics, stainless-steel and HDPE composite IBC totes in the 275-330 gallon range dominate the spec sheet, with stackable 45"x45" footprints cutting floor space by up to 150% versus 55-gallon drums. HDPE suits coolants and detergents, stainless steel fits oils and high-purity
For retail distribution, start with product size, weight, fragility, and sales channel before choosing between folding cartons, rigid boxes, corrugated mailers, kraft boxes, or drawer-style packs; match paperboard grade, flute, and ECT to the channel stresses.
For apparel distribution, storage cages must match SKU profile: carton-flow racks for folded eaches, GOH rails for hanging garments, and modular bin systems for returns and value apparel. Match cage load rating, footprint, and aisle width to the facility's dock and clearance limits before specifying
Air cargo cartons are double-wall corrugated kraft containers (51 ECT / 350# burst) sized to airline ULD and pallet grids. Choose EH or E styles by cubic volume, match ECT rating to stack height, and verify airline + IATA dangerous-goods compliance.
Port-logistics carton selection is now driven by dimensional-weight freight tiers, flute-grade compression ratings, and FSC-certified fiber specs, not by box count alone. Standard catalog 3-ply single-wall kraft (215 GSM, 3 mm) holds 5–10 kg, while double-wall ECT 32–90 lb/in corrugated governs pall
Composite (HDPE inner, steel-caged) IBC totes sized 1000 L within the 275-330 gal plastic / 350-793 gal stainless range dominate air-cargo selection, subject to IATA DGR for hazmat and proper pallet restraint. UN and FDA markings, plus 49 CFR 180.352 retest cadence, gate acceptance.
UN-rated corrugated boxes remain the default UN-certified outer package for shipping most classes of dangerous goods, provided the box passes stacking, leakproofness, hydrostatic pressure, drop, and vibration tests and is rebuilt every 12 months. ECT is now the more common rating vs. Mullen, with do
DEA-compliant storage cages for Schedule III-V controlled substances must use flush-to-floor welded wire panels, self-closing/self-locking doors, and brazed hardware per Title 21 CFR Sections 1301.72-1301.76. Schedule I-II requires vault construction instead of wire cages.
For automotive parts logistics, double-wall corrugated cartons, corrugated bulk containers, and foldable plastic pallet boxes each fit a defined duty band; box selection is dictated by part weight, surface finish, ESD exposure, and returnable-vs-one-way flow rather than by carton style alone.
For food and beverage SKUs, pick corrugated by ECT/BCT and board composition first, then folding carton by closure style. Recycled corrugated held 70% of 2024 material share, RSC 50% of box share, Asia-Pacific 38%.
For electronics handling, specify a Type D FIBC (CROHMIQ or equivalent) with a dissipative liner, food-grade virgin polypropylene fabric, and a 5:1 safety factor at 1,000-2,000 lb capacity, since any spark or contaminant event destroys the load. Class C only if a verified ground point exists at ever
Air-cargo strapping selection hinges on TSO-C172 cargo restraint strap assemblies as the regulatory baseline, with FAA AC120-85A Section 2.8 governing special cargo and IATA ULDR OS 6/07 setting attachment-point spacing rules. Composite woven polyester typically outperforms steel for irregular air-c
For retail liquid distribution, the practical IBC selection is a 275 or 330 gallon HDPE composite tote on a galvanized steel pallet, UN 31HA1/Y rated for the specific gravity of the product, sized to a 45 by 45 inch base footprint that fits a standard GMA pallet rack and a single forklift pocket. St
FIBC bulk bag selection for e-commerce fulfillment hinges on matching Type A-D static control, 500-4,000 lb capacity, and 5:1/6:1 safety factors to product hazard class, with food-grade liners and UN 13/H2/Y certification driving compliance for direct-to-consumer shipping.
PET strapping at 9-19 mm width with embossed or smooth surface is the dominant pick for palletised electronics handling, replacing steel where the load is under ~1,200 kg. ESD considerations, edge pressure on cartons, and tooling (battery or pneumatic tensioner) decide the final pick between PP, PET
Food grade FIBC bulk bags for food and beverage use are woven polypropylene containers built to handle 2,000-4,000 lb loads of dry flowables like flour, sugar, salt, and starch, with selection driven by BRCGS / ISO 22000 food safety certification, bag type (A-D electrostatic class), and clean-room m
Polyester (PET) strapping is the dominant choice for pharmaceutical pallet and heavy-case unitization because retained tension and shock absorption outperform PP and avoid steel's contamination and injury risks. Compliance hinges on FDA 21 CFR Part 211 documentation, ISTA/ASTM transit testing, and F
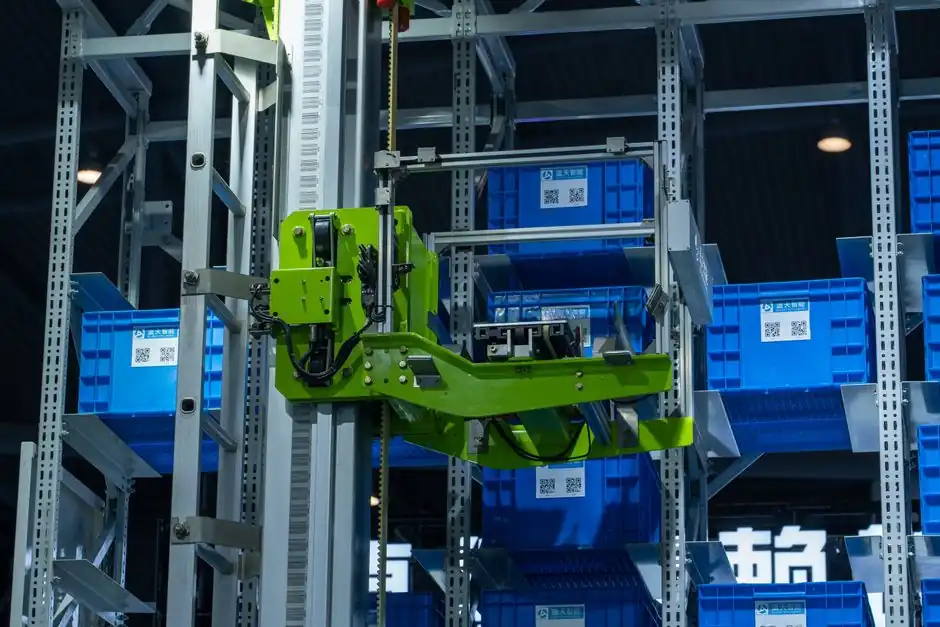
For warehouse automation, select IBC tanks sized at 275 or 330 gallons on a standardized 45" x 45" base, built from HDPE, composite, or 304/316L stainless steel, with UN/DOT transport certification and integrated tracking to integrate cleanly with automated filling and discharge lines.
PP strapping covers roughly 65% of light-to-medium food and beverage bundling, with PET used for heavier outdoor pallet loads; selection hinges on load weight, weld strength, and wash-down compatibility.
Air-cargo stretch film selection balances gauge (24-120 ga, LLDPE), manufacturing process (cast vs blown), and the cargo environment (UVI, VCI, anti-static). Use 80-100 ga cast or blown machine film with UVI additives for typical ULD palletized freight; switch to reinforced blown 100+ ga or netting
PET polyester strapping band selection for port logistics: 12-32 mm widths, 186-1,400 Kgf break strength, 406 mm core, EU PPWR-compliant. PET now covers 68% of European heavy-duty packaging, replacing steel for most pallet, container and break-bulk securing at terminals.
Stretch film selection for warehouse automation hinges on matching gauge, manufacturing process, and pre-stretch yield to the load profile and machine class. Automated wrappers running cast or hybrid cast film at 60 to 120 gauge typically deliver the best cost-per-pallet ROI for distribution centers
Electronics-grade IBC selection pivots on electrostatic control and ultra-clean interior finishes, not commodity chemical compatibility. HDPE bottles with conductive additives in 275/330-gallon form factors are the working baseline, paired with stainless 316L for high-purity process loops.
For apparel distribution, machine-grade cast LLDPE stretch film in the 60-80 gauge range with 200-250% pre-stretch delivers the best balance of clarity, barcode scanability, and load containment on uniform cartons. Blown film (80-120 gauge) is reserved for irregular Type C retail store pallets with
Anti-static LLDPE stretch film in the 40-80 gauge range is the default specification for wrapping ESD-sensitive electronics, with cast film preferred for clarity-driven scanning and blown film reserved for sharp-edged or heavy loads above 2,400 lb. Selection hinges on five criteria: static-dissipati
Automotive parts logistics typically demands Type B/C stretch film with high puncture resistance, machine-grade pre-stretch, and verified load containment per EUMOS 40509 and ISTA 3E. Spec the film first, then the wrapper.
PET and high-tensile steel strapping dominate chemical shipping loads over 1,000 lb, while PP and textile bands cover lighter hazmat-class cartons. Material, width, and joint choice depend on load weight, UV or chemical exposure, and transit distance.
Carton box selection in a 2026 automated warehouse hinges on running WMS cartonization against three live inputs (SKU cube/weight, carrier DIM-weight rules, real-time carton inventory) and pairing that logic with an on-demand box erector. Operations shipping 1,500 to 2,000+ parcels per day see measu
For electronics handling, select single-wall or double-wall corrugated RSC cartons with anti-static/ESD-safe coatings, matching ECT or Mullen burst rating to product mass and stacking load. The market is projected at USD 13.34 billion in 2026, growing at 6.63% CAGR through 2035.
For e-commerce fulfillment, specify LLDPE stretch film in the 8 to 15 micron range, paired to daily parcel volume: hand rolls at 2 to 5 kg for sub-5-ton operations, machine rolls at 10 to 18 kg for 8 to 10 ton throughput, and switch to fully automatic lines only when labor cost makes manual core loa
For retail distribution, plastic turnover boxes dominate the global reusable container market at over 60% share, with the broader turnover box market valued at USD 3.87 billion in 2025 and projected to reach USD 4.07 billion in 2026 at a 5.2% CAGR. Selection should prioritize material compatibility,
Steel storage cages for chemical shipping must be selected by hazard class and package geometry first, with non-combustible construction, liquid-tight spill containment, and segregation by compatibility governing IBC, drum, and tote enclosures.
Air cargo selection now hinges on a Total Cost of Logistics frame: a turnover box is the right pick when shipment value density is high, dimensional weight is under 5,000 kg per ULD, and the lane is time-critical. Choose rigid PP or HDPE collapsible bins over corrugated for any closed-loop route abo
Selecting turnover boxes for warehouse automation requires matching footprint, dynamic load, and stack ratio to the AMR or AS/RS system. Standard 600x400 mm and 400x300 mm footprints with 20-30 kg payload cover most AMR tote flows in 2026 builds.
For cold chain logistics in 2026, the right IBC tank is an HDPE-bodied 275 or 330 gallon unit with a galvanized steel cage, stainless 304/316L valve hardware, and refrigerated-grade AS/RS compatibility, sized to fit 45" x 45" pallet grids and matched to the cold-soak tolerance of the product being s
For apparel distribution, choose turnover boxes by matching footprint, dynamic load rating, and wall material to your SKU mix, slotting density, and shuttle/AMR handling requirements. Folding carton, corrugated mailer, and rigid box formats dominate the 2026 market, each with distinct compression, s
Electronics-grade turnover boxes pair injection-molded or PP-corrugated ESD plastic (surface resistance 10^3-10^9 ohm) with role-defined handoffs; selection hinges on board envelope, route and EPA boundary, not the label "ESD-safe."
Chemical shipping turnover boxes must be UN-specification performance packaging under 49 CFR Part 178, with fiberboard variants passing Cobb, stacking, drop, hydrostatic, leakproofness, and vibration tests, plus mandatory hazard-communication marks and overpack labelling at 0.5 inch minimum text hei
Automotive turnover box selection for parts logistics hinges on matching a standardized container's load rating, footprint, and material to the production-flow role it serves. The global market reached USD 1,931.60 million in 2024, and is forecast to grow to USD 3,803.96 million by 2032 at an 8.23%
Retail-distribution stretch film selection hinges on load type, gauge, and stretch method, with LLDPE machine film at 250% pre-stretch the default for retail DCs handling irregular Type B/C loads.
Food-grade turnover boxes in 2026 are spec'd by contact-surface material (HDPE, PP, stainless AISI 304/316), temperature window, load rating, and stackability, with HDPE dominating cold-chain and produce handling. Selection is driven by inventory turnover ratios of 4-8x in F&B and FIFO-compatible ge
Carton box selection for e-commerce fulfillment hinges on matching board grade, flute type, and inner dimensions to the SKU mix, with corrugated single-wall B-flute dominating small-parcel flows and double-wall BC specified for items above ~18 kg or 60 cm edge length. Standard FEFCO 0201 RSC dies co
Turnover box selection for cold chain logistics is a material-and-temperature specification problem, not a generic plastic-bin purchase: HDPE walls, insulation, and food-grade certifications must match a defined product band from +2°C to cryogenic below -150°C.
Turnover boxes for e-commerce fulfillment should be selected by matching footprint, dynamic load rating, and HDPE grade to the specific picking model. For high-SKU 3PL operations, 600x400 mm vented boxes at 30-50 L with ESD-safe or food-grade options, 25-30 kg dynamic load capacity, and 5,000+ cycle
Retail distribution plastic pallet selection hinges on five engineering decisions: footprint (GMA 48"x40" vs 30"x42" DSD vs EUR1 1200x1000 mm), rated capacity across static, dynamic, and racking states, resin (HDPE vs PP vs recycled), construction (injection molded vs structural foam), and stackable
IBC tank selection for chemical shipping hinges on three concrete decisions: material (HDPE, stainless steel, or carbon steel), capacity band (275-330 gal or 500-1,500 L), and certification scope (UN/DOT 49 CFR 180.352, NSF/ANSI 61, FDA Title 21). Matching these to the chemical class and shipment fr
Plastic pallet selection for warehouse automation hinges on dimensional tolerance, deck stiffness, and bottom-deck geometry matched to AS/RS shuttle and conveyor specs. Standard footprints 1200×1000 mm and 1200×1200 mm dominate European ASRS builds, with maximum deflection of 0.5 in (12.7 mm) under
Cold-chain stretch film must be specified for sub-zero service: LLDPE blown or cold-grade cast films in the 17–23 µm range retain elasticity below 0°C, while standard 15–25°C-grade films crack and lose memory at -20°C. Selection pivots on resin blend, pre-stretch ratio, cling type, and pallet-wrap p
For apparel distribution, choose HDPE or PP injection-molded plastic pallets in the 48"x40" GMA or 1200x1000 mm EUR1 footprint, with static, dynamic, and racking load ratings matched to the SKU weight, ISO 9001-certified manufacturer, and sealed hygienic surfaces. Avoid structural foam and high-recy
Anti-static plastic pallets for electronics handling are defined by measurable surface resistance, not by color or generic ESD labels. Procurement should target static dissipative 10^5-10^9 ohm or conductive 10^2-10^4 ohm ranges, grounded PCBA magazine paths, and full-route ESD mapping.
Passive insulated cartons for cold chain should be selected by payload, route, and evidence, not catalog labels. EPS, PUF, and VIP cores deliver 24h, 48h, and 120h holds respectively, with a 50 kg per-carton handling cap and WHO Class A/B/C temperature bands as the baseline decision set.
HDPE and PP plastic pallets, typically 22 kg versus 40 kg for wood, dominate chemical shipping because they bypass ISPM-15, resist moisture and weak acids, and last up to 10 years. Specify by exposure route, not by a generic chemical-resistant label.
Plastic pallet selection for automotive parts logistics centers on the 48x45 in footprint, HDPE or PP construction, and matched bulk container or KLT integration. Specifying automotive plastic pallets requires verifying dynamic load rating, deck style, and compatibility with rack, conveyor, and just
HDPE/PP injection-molded plastic pallets, sized to GMA 48x40 in or EUR/ISO 1200x1000 mm, are the dominant specification for pharmaceutical distribution, replacing wood to avoid ISPM-15 fumigation, moisture absorption, and microbial contamination. Selection pivots on static, dynamic, and racking load
For cold-chain operations in the -30°C to 0°C range, HDPE pallets are the most widely specified plastic option, with PP as a secondary choice. Material grade, reinforcement layout, and deck geometry must be locked per temperature zone; mesh decks suit quick-freeze tunnels, full flat decks suit fresh
Food-grade plastic pallets for food and beverage plants are made from virgin HDPE or PP, carry FDA/USDA acceptance for direct food contact, and are specified on four axes: material grade, hygienic surface design, dynamic and static load rating, and environmental resistance (cold chain, wash-down, ch
Plastic pallet selection for port logistics is driven by three non-negotiables: ISPM-15 exemption, dimensional fit to ISO 6780/standard footprints, and material choice (HDPE for cold-chain impact resistance, PP for higher rigidity), per 2025-2026 OEM guidance.
Plastic pallet selection for e-commerce fulfillment hinges on five spec gates: footprint (GMA 48x40 in or EUR 1200x800/1000 mm), static/dynamic/racking load rating, material (HDPE, PP, injection-molded), deck style, and ISPM-15 export compliance. Match these against SKU weight, conveyor/automation c
Food and beverage palletizers choose stretch film by load profile: LLDPE cast or blown hand/machine grades for dry goods, vented films for fresh or warm loads, and downgauged high-performance grades for cold-chain and beverage applications. Specs prioritize gauge, pre-stretch, holding force, and foo
Air cargo bench and platform scales are 10,000-30,000 lb capacity deck scales, typically 10'x10' drive-over or LD3 roller formats, calibrated for ULD dollies and parcel feeders. Selection hinges on ULD type, accuracy, indicator protocol, and NTEP/OCI traceability.
Bench scales for port logistics are typically specified at 30-300 kg capacity with 0.2-200 g readability, sitting in a 3 kg-3000 kg envelope for industrial models. For port and sea freight, they sit alongside forklift and floor scales, not as a replacement, handling small parcels, documents, and par
Pharmaceutical carton selection starts with board grade, flute profile, and Edge Crush Test values matched to pallet-stack load, then layered with FMD/DSCSA serialization and cGMP clean-room handling per 21 CFR Part 211. Corrugated RSC at 55% market share and single-wall board at 62% dominate 2024 s
Bench scales for warehouse automation are compact, 6-600 kg capacity tabletop units with 0.01-0.1 kg readability that integrate with WMS, dimensioning systems, and shipping software. Selection is driven by capacity, IP rating, hazardous-area certification, and connectivity protocol.
Bench scales for apparel distribution are typically specified at 6-150 kg capacity, 0.01-0.1 kg readability, IP65 stainless platforms, with NTEP or OIML trade approval and Ethernet/USB data output for carton, hanger, and piece-count workflows.
Specifying FIBC bulk bags for automotive parts logistics means matching Type A-D static control, 5:1 or 6:1 safety factor, and 500-4,000 lb capacity to resin, powder, or component flows under post-JIT buffer-stock rules. Type C with groundable loops covers flammable solvents, Type D handles dusty po
For chemical shipping, a stainless-steel bench scale rated IP68/IP69K with 316 platform, hermetically sealed load cell, and trade-approved readability is the minimum spec; capacity should be sized to the heaviest container plus 25-50% headroom and verified against the chemical's corrosivity and wash
Bench scales for automotive parts logistics are typically specified at 30–600 kg capacity, 0.01–0.1 kg readability, stainless or powder-coated steel platforms, and IP65–IP68 ratings, with ISTA 3A-tested packaging tied to JIT/JIS delivery. A wrongly sized bench scale risks $10,000-per-minute line-sto
For port logistics, HDPE or PP turnover boxes with 1.0-3.0 ton dynamic load, -30°C to 80°C service range, and foldable/nestable designs cut reverse-logistics volume by 40-60% and extend service life 5-8x versus corrugated cardboard, per current manufacturer data.
For European cold-chain pallets between -30°C and +50°C, virgin-grade PP strapping (5-18 mm wide, 38-188 Kgf break strength) is the cost-effective default; PET (up to 1,200 kg) suits heavy loads, while steel and composite are reserved for extreme-duty or sharp-edged cargo. Below -20°C, specify cold-
Food and beverage processors select bench scales by matching IP rating, capacity, and material to the line: 30–100 lb receiving, 5–50 lb portioning, and IP65/IP69k stainless for washdown zones. Choose precision monobloc load cells for recipe work and checkweighers for fill verification.
Bench scales for cold chain logistics should pair NTEP-certified load cells with 304/316 stainless platforms, IP66+ sealing, and a cold-rated operating window down to -20 °C or below. Specify capacity, platform size, and readout type against the SKU mix and pallet flow on the line, not by ambient te
Bench scales for e-commerce fulfillment are specified by capacity, readability, and platform integration rather than by capacity alone; a 0.1 g to 0.01 kg readability band, multi-platform WMS API support, and a 6 kg to 150 kg capacity range cover most pick-and-pack and shipping-validation use cases.
Bench scales for retail distribution are compact, legal-for-trade capable units spanning roughly 0.5 kg to 150 kg, with digital connectivity, IP-rated washdown, and NTEP/OIML certification as the core selection gates. For a retail counter, plan capacity at 1.5-2x the heaviest single SKU, choose a st
Port logistics weighing is anchored by the SOLAS verified gross mass rule and three scale families (weighbridge, forklift scale, floor/bench scale) chosen by container flow, accuracy class, and deployment mode.
Food-grade IBC totes in the 110–793 gal range, built in HDPE or stainless steel, are the workhorse for liquids, syrups, dairy, juice, and wine in modern processing. FDA- and USDA-aligned stainless steel IBCs with sanitary tri-clamp fittings, passivated welds, and 2B finishes are the default for sani
Storage cage selection for retail distribution hinges on five spec variables: wire gauge (6 vs 10 gauge steel), mesh type (woven vs welded), frame profile, finish (galvanized vs powder-coated), and stackability. Match these to inventory value, aisle width, and whether the cage is stationary or reloc
Electronics-handling filling scales should be selected on resolution, platform hygiene, and digital interface, not raw capacity; bench-scale formats below 30 kg with 0.1–10 g resolution cover most SMT and semiconductor sub-pack dosing.
Chemical shipping scales are selected by combining platform capacity with product-contact material compatibility (304/316 SS, HDPE, PP, PTFE), then matching fill technology to viscosity: gravity under ~100 cP, pump 100–5,000 cP, piston above 5,000 cP.
Filling scales for automotive parts logistics are chosen around four hard constraints: per-batch part mass, container tare, just-in-time 30-minute delivery windows, and 2.3% baseline damage on electronics. Right-sizing scale capacity and resolution against these gates cuts rework and supports market
For pharmaceutical distribution, pick a filling weighing scale by matching dose mass, accuracy class and OIML R76 or USP <41>/<1251> tolerance to product risk: peristaltic or servo-piston fillers with load-cell checkweighing suit 0.1–500 mL doses, while gravimetric net-weight fillers dominate above
Food and beverage filling scale selection runs on three decision gates: product viscosity, container format, and washdown/IP rating. Piston fillers dominate viscous sauces at 10-100 bottles/min, while flow meter and load cell fillers target liquid accuracy in regulated lines.
Pick a filling scale for cold chain logistics on temperature tolerance, IP rating, and weighing resolution first, then checkweigher throughput. Filling scales in cold rooms should be stainless 304/316, IP65+ rated, and resolution of 0.1–1 g for pharma or 5–50 g for food. Skip them for sub-zero weigh
For retail distribution, specify a dynamic checkweigher in the 1-12 kg range with OIML R51/MID approval, IP65+ washdown rating, automatic mean-weight correction, and 100% in-line inspection at throughput of 100+ packs per minute to satisfy BRC, IFS, and retailer chargeback requirements.
For air cargo, select a checkweigher rated for palletised loads of 100-3000 kg with IP65 or higher protection, ATEX/IECEx certification if placed in fuel-adjacent zones, dynamic accuracy of 0.05-0.1% and conveyor integration matching ULD handling speed at 0.5-2.0 m/s. Roller-top or belt-top platform
Port logistics checkweighers in the 50 g to 300 kg class are typically specified at ±0.1% or ±5 g accuracy, 0.3 to 2 second cycle times, and integrated with 1D/2D/RFID scanning to catch underweight parcels before they hit the container. Selection hinges on capacity band, legal-for-trade status, and
Automatic checkweighers for warehouse automation should be selected on through-line speed, accuracy class, IP/NSF rating, and reject-system integration, with global market value projected at USD 357.9 million by 2035 at a 2.5% CAGR. Specs like ±0.5 kg at full line speed with PLC interlock to AG
For electronics packing lines, specify dynamic checkweighers with anti-static guarding, ≥0.1 g resolution, and throughput headroom 15-20% above peak. Reject a unit that cannot handle ESD drift on the weigh belt, ships without upper/lower feedback to fillers, or relies on bench-top sampling above ~20
Chemical shipping demands ATEX/IECEx certified checkweighers with Hastelloy or PTFE contact surfaces, IP66/IP69K enclosures, and accuracy class IIIL to I for solvent, acid, and powder loads.
Pharmaceutical checkweighers must hold ±50 mg accuracy at 3-sigma and run above 150 ppm to satisfy GMP and 21 CFR Part 211 dose-Integrity requirements. Selection hinges on five gates: weighing range, accuracy class, hygienic build, reject mechanism, and line-speed match against your SKU mix.
Selecting a checkweigher for food and beverage lines hinges on six spec gates: resolution class, total weight range, throughput, IP rating, rejection mechanism, and line integration. Match the OIML R76 accuracy class and the wet-area ingress protection to the product and washdown regime before evalu
Cold chain checkweighers are typically stainless IP65/IP69K dynamic units paired with metal or X-ray inspection, sized to conveyor speed (30-600+ ppm), tare window, and the legal-for-trade accuracy class your HACCP/QMS demands.
For air cargo weighing, specify a truck scale (pit-type, 30-80 t, ±0.05% accuracy) when single-piece ULD/PGA loads cross 1,500 kg or when total consignment exceeds 6,000 kg; below that, platform or pallet-jack scales are sufficient.
Port-logistics truck scale selection turns on four specs: 18 m / 80 t deck, OIML R76 Class III multi-interval accuracy, IP69K digital load cell network, and pit or above-ground profile matched to gate throughput. Add chloride-resistant deck finish and a redundant diagnostic path when the site is wit
For warehouse automation, pair a fixed weighbridge (Class III, 50-100 t, 12-18 m platform) for inbound/outbound trucks with a 2-3 t IP65/IP67 pallet truck scale at the picking floor to cut 30-60 seconds per pallet and feed WMS data directly.
Chemical-plant truck scale selection hinges on matching load-cell technology, hazardous-area classification, and DOT compliance. Pit or surface configurations, NTEP-certified indicators, and 80,684 USD-per-violation DOT fines drive the spec.
Automotive-parts truck scale selection in 2026 hinges on matching platform length (12-18 m for medium-to-heavy trucks), Class III accuracy with 10 kg scale interval, and legal-for-trade certification to inbound, outbound, and FVL flows.
Food-grade truck scale selection hinges on NTEP Class III certification under NIST Handbook 44, IP66-69K washdown enclosures, and stainless or galvanized load cells sized to the heaviest inbound tanker plus a 10-20% capacity buffer. Pit or surface mounting is decided by sanitation drainage and appro
E-commerce fulfillment truck scales are specified by three concrete gates: weighing capacity equal to Gross Vehicle Weight plus a 5%–20% buffer, platform length 1.5 m longer than the longest wheelbase, and OIML R76 or NTEP certification for legal-for-trade billing.
Carton erecting machines for air-cargo hubs must match 25–40 cases/min throughput, 200–550 mm carton length, 0.6–0.7 MPa plant air, and 48–75 mm tape. Fixed-size units beat changeover delays, while inline-ready 25TB-class models fit 24/7 sortation lines.
For 2026 port-logistics carton erector selection, spec the machine at 1.3× net downstream throughput, choose double-station full-servo (80-180 cpm) for container-yard duty, and confirm CE certification plus B/C-flute board range. Single-station units (30-50 cpm) fit only low-volume feeders.
For warehouse automation in 2026, select a carton erecting machine on five spec gates: throughput band, blank size envelope, drive and control architecture, changeover time, and downstream hand-off. The 15-40 cpm tier fits 300-3,000 cartons per shift; above that, spec a 50-180 cpm PLC line.
Chemical-shipment carton erecting machines must be specified against three axes: 15-40 cpm entry or 80-180 cpm high-output speed bands, B-flute/C-flute board plus hot-melt glue at 160-180 °C, and 380 V three-phase power with 6 bar ISO 8573-1 class 2.4.2 air.
Pharma-grade automatic cartoning machines for 2026 must satisfy GMP construction, 21 CFR Part 11 serialization, and EU FMD traceability while sustaining 60–200 cartons/min on real SKUs. Selection is driven by five pillars: stainless construction, IQ/OQ/PQ validation, track-and-trace integration, cha
For food and beverage carton erecting, water-glue double-lane erectors at 200-300 boxes/min (Feida ZX-2000) suit large fast-food runs, while dual-channel independent-control models at 600 pcs/min (Dayuan CE1000/2-Bi) handle mixed-SKU plants, and Siemens PLC combo units at 720 cartons/h (YPK-4012) fi
Cold chain carton erecting hinges on three decisions: stainless or food-grade contact parts for washdown, hot melt glue sealing instead of standard tape above 80% RH, and servo-driven format change for mixed-SKU frozen loads. Match these to a rated 15-30 cartons/min erector paired with a uniform ran
An automatic carton erecting machine is the right pick for e-commerce fulfillment centers running above roughly 5,000 orders per day, where case erecting speeds of 1,200-1,500 cases/hour replace manual box forming and clear upstream bottlenecks on the filling line.
For retail distribution in 2026, a vacuum packaging machine is selected on four hard gates, not price: usable chamber volume, ultimate pressure, seal-bar length, and pump displacement. Match architecture (tabletop, double-chamber, continuous-belt, tray-sealer MAP, or thermoform) to daily pack count,
For warehouse automation, choose a vacuum packaging machine by matching chamber architecture, pump capacity, and seal-bar length to your daily pack count, product shape, and washdown duty, with 304 stainless contact parts, 20-40 m³/h pumps, and PLC controls as the baseline spec floor.
For apparel distribution, select a chamber vacuum sealer with 110–160°C sealing range and 8–12 mm seal width for low-volume specialty garments, or a continuous-belt unit at 12–35 pouches/min for ≥500 units/day e-commerce runs, sized to ASTM F2338-22 and ASTM F88 leak-rate gates.
PCB and IC vacuum packaging requires sub-mbar ultimate pressure, dry N2 backfill at 99.995% purity, and ESD-safe chamber construction, not a food-grade chamber sealer. A 20 m3/h rotary-vane pump with a 316L chamber hits 0.5 mbar in 18 seconds and is the realistic floor for Class 3 electronics.
Chamber vacuum packaging with a 20 m³/h rotary-vane pump pulling to roughly 100 Pa is the default 2026 spec for shipping hygroscopic and dust-prone chemicals in 1-50 kg bags, paired with ATEX/IECEx dust-explosion proofing when the powder is combustible.
For automotive parts logistics, choose a floor double-chamber or continuous-belt vacuum packaging machine with a 500-850 mm seal bar, 40-100 m³/h dry pump, 304/316 SS food-grade contact surfaces, and 1.5-2× pump displacement safety margin to protect against transit breakage, oxidation, and humidity.
For pharmaceutical distribution, specify a chamber vacuum packaging machine built to GMP-grade stainless (304 contact, 316 for chloride-bearing APIs), ≤5 mbar ultimate vacuum, and double 950 mm seal bars running 15-45 second cycles. Match machine type to product geometry, not brochure output claims,
Chamber vacuum packers remain the default for food and beverage lines in 2026, with tabletop bell units dominating SME builds. Match architecture to product (chamber vs. external nozzle), pump size, residual pressure capability, and MAP gas flush to avoid overpaying for capacity the line will never
For 2026 cold-chain food processors, a chamber vacuum sealer sized at 100-200 packs/hour (single/double chamber, 304 stainless, Busch or Leybold pump) covers most butcher and central-kitchen duty under $8,000, while continuous belt and thermoforming systems take over above 800 packs/hour. Match mach
For e-commerce fulfillment, select a vacuum packaging machine by four hard gates: chamber working volume, ultimate pressure (around 100 Pa absolute), seal-bar length (400–600 mm covers retail stock), and pump displacement (20–100 m³/h). Double-chamber tables (3–6 cycles/min) and continuous belt seal
For retail distribution in 2026, pick a shrink wrapping machine by matching throughput band to true demand (chamber <50 p/h, L-bar 6–15 p/min, flow-wrapper 30–120 p/min, high-end HFFS 120–180 p/min), then lock film resin (POF 12–25 µm, PE 40–100 µm), tunnel window (160–220 °C POF, 180–240 °C PE), an
Shrink wrapping machines for air cargo are best limited to secondary pallet and ULD-net stabilization at 1.5–9 G load envelopes, with primary air-freight packs relying on ECT >32 lb/in corrugate, air-cushion systems at 15–28 m/min, and honeycomb kraft wrap rated to -20°C holds. Selection hinges on L
Shrink wrapping machines at ports belong to a different equipment class than stretch pallet wrappers; selection turns on film type, throughput, and pallet profile rather than retail appearance.
Warehouse automation demands shrink wrappers selected by accepted-output rate, film type, and tunnel occupancy, not brochure cycle speed. POF film dominates freezer-grade lines; PE fits heavier bundles. Match L-bar, side sealer, or sleeve wrapper to volume, then validate every stage.
Apparel distribution shrink wrapping selection is driven by SKU count, film type (POF vs PE vs PVC), throughput (35-85 ppm on the Prasmatic TC series), and downstream recyclability of pallet wrap; for most garment DC operations, a semi-automatic POF system paired with a stretch-film baler is the low
For chemical shipping, select a shrink wrapping machine with PE 40–100 µm film, a 180–240°C tunnel, a continuous band sealer (≥32 N/15 mm seal strength), and ATEX/IECEx-rated electrics for hazardous-area lines.
For automotive parts logistics, orbital horizontal stretch wrappers with 17.7–85.4 in rings and 2.0 m turntable pallet wrappers with 300% pre-stretch are the two spec lanes engineers lock before quoting, split by part geometry and pallet volume.
Pharma distribution shrink wrapping: match chamber vs L-bar vs automatic sleeve to film temperature window (POF 120-150°C, PVC 140-180°C, PE 160-220°C), throughput (5-60+ packs/min), and FDA 21 CFR Part 11 audit logging. Below 5,000 units/day use semi-automatic; above 10,000 specify full-auto with s
Shrink wrapping machines for cold chain logistics must be selected against three temperature tiers (+2 to +8 °C chilled, -18 to -30 °C frozen, -60 °C and below deep frozen) because PE film loses 30 to 50% of elastic recovery below -20 °C. POF film is the freezer-grade standard; PVC is rejected for c
Shrink wrapping machine selection for e-commerce fulfillment is driven by pack envelope, film resin/gauge, sealer type, and tunnel window; chamber machines handle 4-8 packs/min, side-seal wrappers reach 60-100 packs/min, and dual-lane continuous motion hits 120-200+ packs/min on collation.
For air-cargo case packing, side load units (1-16 cartons/min, 4.5 kW) suit uniform cartons under 500 mm, while top load pick-and-place (1-8 cartons/min, 7.5 kW) handle irregular or longer shippers up to 600 mm. Selection hinges on case format, sustained throughput, air supply (0.5-0.8 MPa), and 380
Port-logistics case packers are specified against FEFCO 0201/0200/0203 case styles, ANSI/PMMI B155.1 and ISO 12100 safety references, and TAPPI T811 ECT / ASTM D642 / ASTM D4169 board validation, with throughput bands from 10 to 200 cases per minute across top-load, side-load, wrap-around, and robot
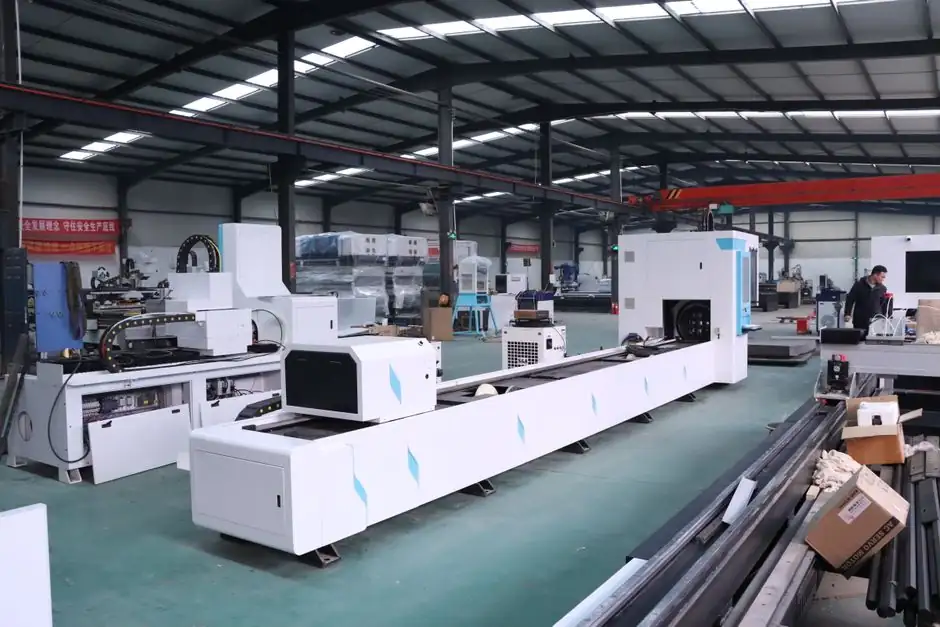
Specifying a case packer for warehouse automation hinges on three measurable axes: case format range, cases-per-minute at the slowest approved SKU, and corrugated-strength compatibility per TAPPI T811 and ASTM D4169. Match the 380V 3-phase, 0.5–0.8 MPa air envelope to your plant utilities before quo
Apparel case packing rejects side-push and wrap-around cells: soft, low-compression-stack garments only run reliably on top-load pick-and-place or robotic cells with 3-15 cpm rated speed and sub-5-minute recipe changeovers, sized against ASTM D642 case compression and a verified SKU mix.
For electronics handling, a case packer must combine anti-static, low-impact product handling with the spec discipline of any secondary-packaging cell: FEFCO case style, ECT-rated corrugated per TAPPI T811, and throughput in cases per minute matched to the upstream SMT line. Top-load and robotic top
Case packing machines for chemical shipping in 2026 are built around stainless contact parts, washdown-rated frames, and ATEX/IECEx options, with top-load, side-load, and robotic architectures selected by container weight, throughput, and UN-rated shipper type. Source data confirms chemical as a nam
For pharmaceutical distribution, specify a servo-driven automatic case packer with ±0.15 mm repeat accuracy, 304 stainless steel contact parts, 99.5% PLC reliability, and full validation documentation against FDA 21 CFR 210/211 and EU GMP Annex 15. Top-load, side-push, and 3-in-1 erect-pack-seal arc
E-commerce case packer selection hinges on three specs: carton size envelope, cases-per-minute after rejects with 20-30% headroom, and a written URS covering TAPPI T811 ECT grade, ASTM D642 compression, and ASTM D4169 / ISTA distribution validation.
Labeling machines for retail distribution in 2026 split into three procurement bands, US$1,500-3,000 for self-adhesive wrap, US$1,600-3,080 for rolling/vertical, and US$4,000-7,000 for semi-automatic benchtop units, with selection gated by container geometry, label stock, throughput, and control int
For air-cargo labeling, specify print-and-apply machines with UDI/IATA-compliant variable data, ±0.5 mm placement accuracy, and 30-300 unit/min throughput matched to ULD build-up, not conveyor lines. Match container first (ULD tag, pallet placard, single-piece tag), then label stock (BS 5609 marine-
Warehouse-automation buyers should match labeling machines to four gates: container geometry, label stock, throughput, and control integration. OPP hot-melt, pressure-sensitive, and sleeve platforms dominate, with throughput targets 40-60% of theoretical maxima. For corrugated cartons, brush/roller
For apparel distribution, select a labeling machine by first matching it to product shape, label format, and required throughput, then verifying placement accuracy of ±1 mm at a realistic 20–60 units/min for mid-volume lines, with tamper-evident and RFID options sized to your label stock and integra
For chemical shipping in 2026, specify a self-adhesive pressure-sensitive (PSA) round-bottle labeler on a 304/316 stainless frame with sealed photoeyes, and confirm container OD, label size and IP rating against the GHS placard, UN packaging mark and lot/date code set before quoting any line speed.
For automotive parts logistics, specify an inline linear labeling machine with servo drive, ±1 mm placement tolerance, and barcode/QR verification on a variable-speed conveyor, matching the SKU mix to throughput windows of 10,000-30,000 units/hour. Validate against test cartons, real labels, and a k
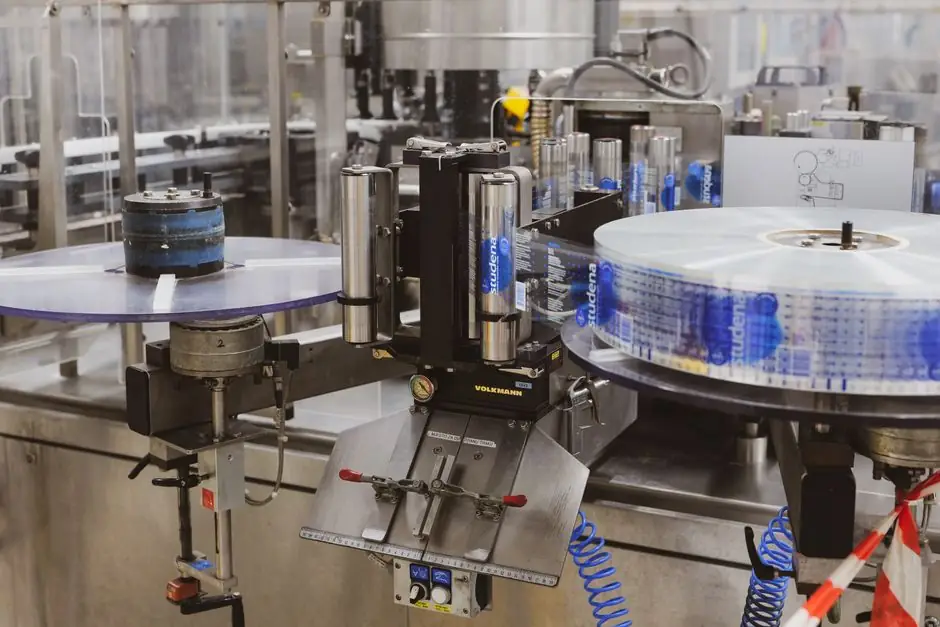
Cold-chain labeling machine selection is driven by three non-negotiable sub-zero specs: ambient-rated operation down to -30°C, condensation-proof IP65+ enclosures, and freezer-grade adhesive/substrate pairing (acrylic deep-freeze to -40°C on PP/PE face stock). Match machine type to container geometr
For e-commerce fulfillment, choose print-and-apply labelers above ~30 cartons/min and pressure-sensitive wipe-on or tamp-blow units for batch picking, matching automation to SKU mix and WMS integration needs.
Retail distribution plants should match capping and sealing machine class to daily volume: manual sealers handle under 1,000 cans/day at $100-500, semi-automatic units cover 1,000-10,000 cans/day at $1,800-5,000, and rotary or monoblock lines serve higher throughputs with induction, impulse, or ultr
For port logistics, automatic capping and sealing machines are selected by closure type (screw, snap, plug, crimp), throughput 30 to 72,000 containers per hour, and torque accuracy within 5 percent, with servo-controlled spindles rated 500 to 3,000 RPM and IP-rated hygienic construction for export-c
Container format and cap principle drive 70% of chemical-shipping capper and sealer specification in 2026, with spindle, chuck, snap and induction head families mapped against torque, ATEX/IECEx zoning and elastomer grade. Specifying EPDM or PTFE seals, IP69K washdown servo enclosures, and torque re
Automatic capping and sealing machines for food and beverage lines typically run 60–300 containers per minute, with servo torque control of 0.5–15 Nm and 15–80 mm cap diameter range. Selection is principle-led (spindle, chuck, snap, ROPP, induction) then head-led then control-led, matched to cap/con
Cold chain capping and sealing machine selection hinges on four gates: IP65+ enclosure, container diameter 30-110 mm, leaker rate under 2%, and torque tolerance ±5%. Match drive type and cap family to the cold-chain SKU before quoting throughput.
Retail distribution filling lines typically pair a volumetric piston or overflow filler with 2-12 nozzles, hitting 20-200 containers per minute and ±0.5-1.0% dosing accuracy on SS304/316 contact parts. Selection is gated by product viscosity, container format, daily volume, and FDA/GMP compliance, w
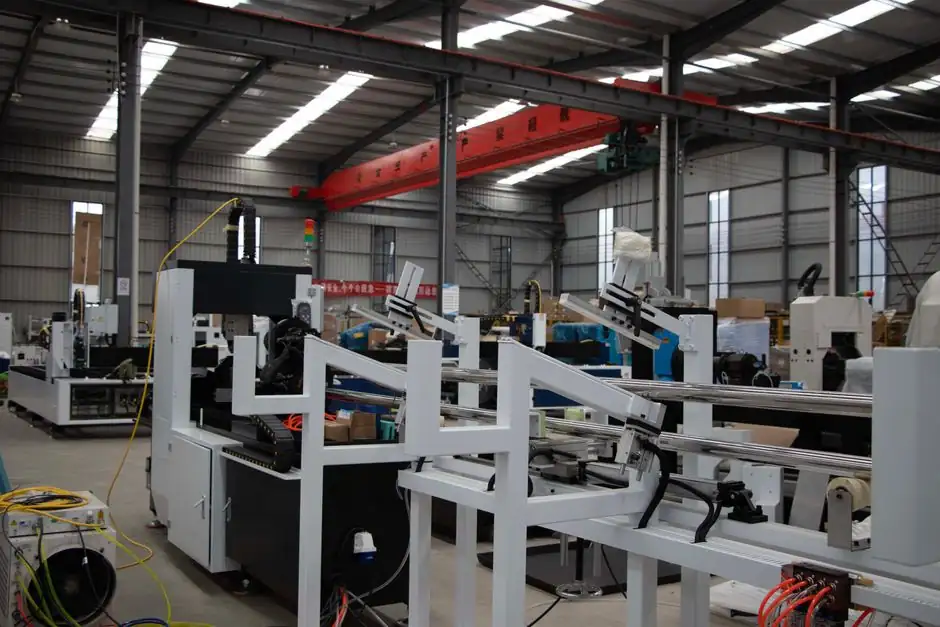
Filling machine selection for warehouse automation in 2026 hinges on matching viscosity (1 to 100,000+ cP), dosing precision (±0.10% to ±0.50%), and CIP/SIP compatibility to a WMS/WCS layer that sequences AS/RS, AMRs, and conveyors. Targets: ≥200 BPM lines with ±0.2% servo-piston repeatability and E
For apparel distribution filling lines, pick a CE-marked pneumatic down/fiber filler with 2-4 scales per nozzle, a 0.1-25 g silo range, 220 V/50 Hz single-phase power around 2 kW, and 200 sets/month throughput.
For chemical shipping operations, the right filling machine is a corrosion-resistant system sized to the container: 316L stainless or PTFE wetted parts, ATEX rating for volatile products, gravimetric accuracy around ±0.1%–1%, and dedicated platforms for 60–250 L drums or IBC totes with load-cell wei
For automotive parts logistics in 2026, a piston or net-weight filling machine with ±0.5 g accuracy, submerged nozzle, and MES trace data handles glycol-based rubber bushing liquids cleanly. Piston for versatility, pump for mid-viscosity, net-weight for premium Tier 1 audit trails.
Pharmaceutical liquid filling line selection is decided by product viscosity, sterile containment class, and the ±0.1–1% accuracy band of the dosing principle, with cGMP, US FDA, and EU-GMP compliance framing every other spec. Match technology (piston, peristaltic, servo pump, net-weigh) to the mole
Filling machine selection for food and beverage in 2026 is governed by four independent spec gates: product state, dosing accuracy, contact-material compatibility, and line throughput. A typical mid-volume European liquid line runs 30 to 120 bottles per minute at ±0.5 to ±1.0% volumetric tolerance,
E-commerce fulfillment runs best on servo-driven piston or net-weigh fillers at 30 to 120 containers per minute, with 76/211/EEC three-packers tolerance, OIML R87 accuracy class, and ATEX 2014/34/EU zoning for aerosols or solvents. Match viscosity, container geometry, and SKU mix before chasing thro
Retail-distribution coders span hot ink roll, ribbon TTO, CIJ, TIJ, and laser; selection pivots on substrate, line speed, and mark permanence, with hot ink roll and TTO dominating 100–600 pcs/min FMCG lines.
For port logistics in 2026, the correct coding machine is a continuous inkjet (CIJ) or thermal transfer overprint (TTO) unit selected by substrate, line speed, and GS1 barcode grade, not by brand. CIJ fits non-porous drums, cans and HDPE crates; TTO fits corrugated cases and shrink film. Both must c
Apparel distribution centres running 500+ units per hour should default to CIJ or TTO coding machines with conveyor integration, while manual contact coders under 50 UPH remain viable for short fashion drops. Selection hinges on substrate, line speed, consumable cost per 1,000 marks, and the GS1 tra
Coding machines for electronics handling in 2026 split three ways: CIJ for curved enclosures, TTO for flexible pouches and labels, and laser for cable jackets and bare metal. Specify by substrate, line speed, IP rating, and 2D DataMatrix grade, not by brand.
For chemical shipping containers, CIJ printers with IP65 enclosures running at 200–450 m/min are the default pick, while laser markers and TTO serve film, drum, and tamper-proof needs. Match ingress protection, substrate, and line speed before brand.
Pharma distribution coding machines must meet FDA/EMA serialization, GS1 barcode legibility, and GMP trace-back rules; TIJ and CIJ lead for vials, TTO for cartons, laser for ampoules. Selection hinges on substrate, line speed, and read-rate, not price.
Coding machine selection for cold chain logistics hinges on three cold-specific requirements: condensation-proof IP65+ enclosures, low-temperature-rated ink (down to -25°C for CIJ, -40°C for laser), and washdown-grade stainless housings that survive daily sanitization. Continuous inkjet fits high-sp
For e-commerce fulfillment operations exceeding 10,000 orders per month, industrial coding machines (CIJ, TIJ, laser) are specified at the packing station to print shipping labels, batch codes, and tracking barcodes on cartons and polybags; selection hinges on substrate, line speed, and DPI, with CI
For retail distribution, specify PET strapping with friction-weld or heat-weld sealing at 200-450 N tension on semi-automatic or automatic machines; PP works only under 30 kg unit loads, while steel is excluded by carton-edge crush risk on mixed-SKU pallets.
Air-cargo pallet strapping requires PP, PET, or steel band matched to ULD air-freight pallets with battery or pneumatic tools for ramp-side use. Throughput targets of 30-60 pallets per hour and tight tension control are the dominant selection drivers in 2026.
Port-logistics strapping machine selection in 2026 hinges on matching PET, PP, polywoven, or steel strap to load weight, port environment, and duty cycle. Cordless battery tools delivering 250-400 cycles per charge, mobile strapping units under 40-second pallet cycles, and stainless-steel corrosion-
Polypropylene (PP) strapping machines are the default spec for apparel distribution: lightweight coils suit mobile workstations, heat-weld sealing is gentler on cartons, and 9-12 mm PP strap handles most parcel and bundle duties at 20-30 straps/min on entry-level semi-auto heads.
For electronics handling, a semi-automatic strapping machine running 9-16 mm PP or PET strap with adjustable electronic tensioning typically fits mid-volume PCB and finished-goods packing, while manual tools cap out well below 100 packs/shift. Match strap width, seal type, and arch size to ESD-safe
For chemical shipping, specify polyester (PET) strapping up to 3000 lb pallet weight and reserve steel only for non-compressible, sharp-edged loads above 4000 lb, with the strapping machine and seal method selected as one matched system.
For automotive parts logistics, select a strapping machine by matching strap material (PET vs PP vs steel), tension range, and automation level to load weight, surface hardness, and throughput. Heavy forged or cast parts typically need PET or steel strapping at 2000-5000 N tension on semi-automatic
Pharmaceutical pallet strapping is governed by Good Distribution Practice: PET strap (not steel), sealless friction weld, repeatable calibrated tension, and low-contact automated routing are the four non-negotiables for cold-chain loads in 2026.
Food and beverage strapping runs on PP or PET, never steel, because cold-chain condensation, washdown chemistry, and FSMA traceability rules make metal strapping a contamination and recall risk. Specify stainless frames, IP65 sealing heads, and low-tension PET for pallet unit loads over 250 kg.
E-commerce fulfillment operations select strapping machines by matching daily order volume, package size range, and integration depth: tabletop semi-automatic units fit under 30 packages per shift, automatic inline machines serve 50+ bags per minute, and battery tools cover off-station pallet loads.
Retail distribution wrapping equipment splits into three main families: side-seal shrink wrappers for individual retail units, flow wrappers for high-SKU confectionery and bakery, and stretch wrappers for pallet loads up to 4,400 lb. Pick by SKU mix, throughput, and tamper-evidence duty, not by film
For air cargo wrapping, match the machine to the operating envelope: IATA ULD sizes (LD3/LD7/LD11) for shape, 9 G downward acceleration for force, and 1.5–9 G vibration loads for cushioning. Use double-wall corrugated (ECT > 32 lb/in), UN-certified packaging for dangerous goods, and GDP-qualified in
Port-logistics wrapping machine selection in 2026 hinges on three machine families, turntable stretch wrappers with powered pre-stretch carriages, semi-automatic pallet wrappers, and supporting strapping and carton sealing lines, matched to LCL consolidation, container export, and pallet-load throug
Warehouse operators should match a pallet wrapper type to shipment volume and load geometry: semi-automatic turntable for under 30 pallets/hour, rotary arm for unstable tall loads, and fully automatic ring/conveyor systems for 60+ pallets/hour. Selecting on throughput, film savings (10–30% vs manual
Apparel and textile roll wrapping machines are selected by product geometry, throughput, and pre-stretch ratio: radial/axial reel wrappers handle OD 400–1200 mm fabric rolls at 10–60 rolls/hr, while turntable pallet stretch wrappers handle unitised cartons at 20–40 pallets/hr with a 200–300% pre-str
For electronics handling, a wrapping machine is selected by matching ESD-safe film, package geometry, and throughput: semi-automatic rotary-table stretch wrappers suit 50-300 pallets/day, while flow wrappers handle individual PCB and device packs. Use the criteria below to pick between semi-auto str
Orbital horizontal stretch wrappers (ring sizes 17.7-85.4 in, 90 RPM) handle long automotive parts where turntables fail, while 2.0 m turntable pallet wrappers with 300% pre-stretch suit boxed components at 500+ pallets/day.
Pharma distribution wrapping decisions hinge on matching film sealing method, line speed and validation to 21 CFR 210-211 CGMP rather than chasing throughput alone. Automatic HFFS flow wrappers (40-100+ packs/min) suit unit-dose sachets; shrink bundlers handle outer multi-pack format for cartons and
For 2026 food and beverage lines, a wrapping machine is selected by matching product form (solid bar, powder, liquid, pallet load) to one of four platforms: flow wrapper (HFFS), rigid-container line, pallet stretch wrapper, or shrink system. Flow wrappers and pallet wrappers dominate the spec data r
Wrapping machine selection for cold chain logistics in 2026 hinges on matching stretch film formulation and pallet containment force to temperature tiers (+2 to +8 °C chilled, -18 to -30 °C frozen, -60 °C deep frozen), because PE film loses elasticity below -20 °C and load stability drives total col
For retail distribution in 2026, match order picker class to pick height and SKU profile: low-level units (2.5–2.8 m lift) for case picking, mid-level (3–6 m) for mixed-SKU retail, with retail-DC benchmarks of 80–150 cases/hour and a $21.50/hr U.S. operator wage point as cost reference.
Air-cargo order picking is dominated by low-level electric order pickers rated around 500 lb platform capacity and 138 inch platform lift, with operators requiring RF scanner, pallet jack, and 30-50 lb lift capability per recent job specs.
Order picker selection for port logistics hinges on three hard constraints: working aisle width (typically 2.8-3.5 m), platform lift height matched to racking tier (4.5-7.5 m), and a chassis rated for the mixed-cycle duty of quay-side, container-freight-station, and bonded-warehouse operation. Lithi
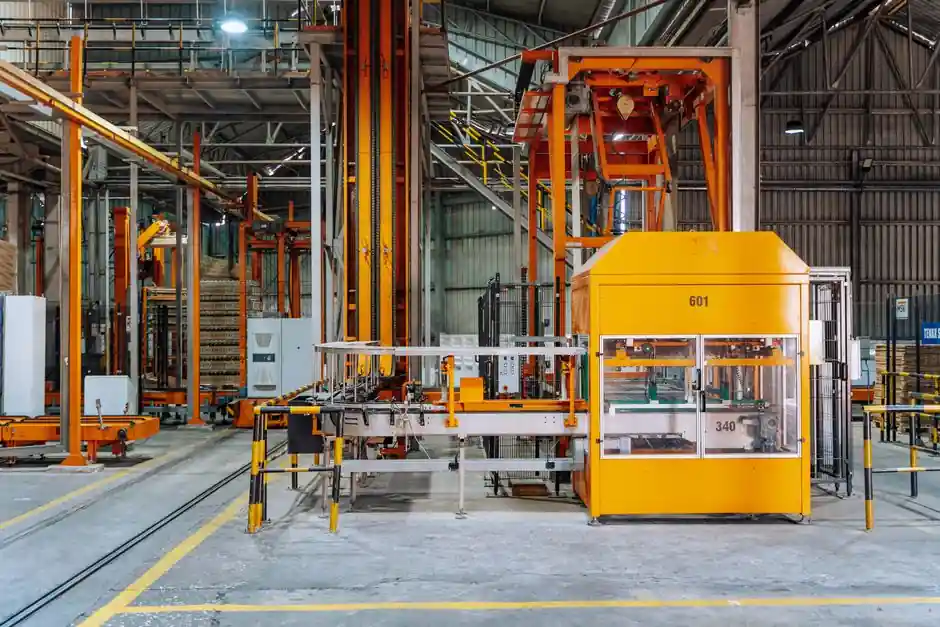
Order picker selection pivots on three quantifiable criteria: pick height (typically 2.5–10 m for standard units, higher for man-up models), aisle width relative to load footprint, and whether the workflow is piece, case, or batch picking. E-commerce and grocery DC operations consistently favour low
Apparel-distribution order picker selection hinges on matching lift height, platform width, and battery class to garment SKU profiles: 2.5–3.5 m order pickers dominate narrow-aisle picking, while full-pallet garment handlers sit at 1.2–1.8 m. Wages of $18.00–$21.50/hr and incentive-bonus structures
For electronics handling, specify a low-to-mid level electric order picker (lift height ≤6 m), anti-static platform and wheel materials, Li-ion power, and zone picking for traceable SKU accuracy above 99%.
For automotive parts logistics, mid-level order pickers with 3–6 m platform lift, lithium-ion power, and WMS integration are the dominant spec. Match machine class to SKU profile, aisle width, and picking height, not to brand.
Pharmaceutical distribution order pickers run mostly in refrigerated 2–8°C zones with regulated pick-face, lot, and expiry controls, and most U.S. sites currently pay pickers $16–26/hr per CVS Health postings (2026-07-14). The wrong picker class on a pharma DC floor can add mispick costs averag
Food and beverage warehouses need order pickers rated for washdown, stainless or food-grade contact surfaces, freezer-class batteries below 0 °C, and lift heights matched to rack tiers, with 24V or 36V electric models the common baseline.
Order picker selection for cold chain hinges on matching lift height, battery chemistry, and operator PPE to sub-zero work zones like -5°F freezers. Electric narrow-aisle stockpickers (24V/36V) dominate frozen and dairy aisles, while ride-on pallet jacks cover ground-level dry cooler picks.
For e-commerce fulfillment, order picker selection is driven by pick height, aisle layout, and order profile: OPC-03 (3 m) and OPC-04 (4 m) self-propelled units cover most SKUs, while batch, zone, or cluster picking methods must match throughput targets. Spherion's July 2026 Los Angeles listing at $
Reach trucks lift up to 12 m in 1.6-2.0 t configurations and operate in 8.5-9.5 ft aisles, making them the default narrow-aisle choice for retail distribution centers handling high SKU turnover. Selection hinges on mast height, load profile, and battery duty cycle. This article maps specs, compariso
Reach trucks are battery-powered narrow-aisle forklifts that lift pallets beyond 10 m in indoor warehouses, but air-cargo terminal duty drives specs toward ULD-rated chassis, side-loading reach, and multidirectional capability. For air-cargo handling, choose a reach truck when racked ULD storage exi
Reach trucks serve port logistics only in specific zones: high-bay cross-dock sheds and empty-container depots needing 2.4-3.0 m aisles, where a 12 m lift and indoor-rated electric chassis are required, not the outdoor heavy-lift work performed by reach stackers (10-46 t) and loaded container handle
Reach trucks are narrow-aisle electric lift trucks built for high-density pallet racking, with pantograph reach, 8-10 ft aisle fit, 20-40+ ft lift height, and 3,000-6,500 lb capacity. They suit indoor put-away/retrieval; counterbalanced forklifts remain better for outdoor, dock, and heavy-pallet wor
Reach trucks in the 1,400-1,800 kg class with 2.7-3.2 m aisle capability and lift heights up to 11 m are the default spec for electronics distribution aisles above 6 m. Below 6 m rack height, a counterbalance electric forklift in a 3.5-4.5 m aisle is usually cheaper. ESD-sensitive electronics storag
Pharmaceutical distribution centers typically select 1.5–2.0 ton electric stand-up reach trucks with 8–10 ft aisle compatibility and 20–40+ ft lift height, prioritizing zero-emission electric power and GMP-friendly finishes over heavier 2.5 ton units.
Reach trucks in the 1.6–2.0 t class, with lift heights up to 12.0 m, suit narrow-aisle food and beverage warehouses running over 3,000 SKUs, provided the build is food-grade and cold-store rated. Electric powertrains cut indoor emissions for HACCP compliance, while chassis, mast and battery spec sti
For cold chain warehouses operating between -25°C and +4°C, a 1.6-2.0 ton electric reach truck with a cold-store conditioning package is the spec baseline; aisle width must stay at or below 2.8 m, lift height at 6.0-9.0 m, and operators must be limited to 60-90 minute shifts in the freezer zone.
Reach trucks for e-commerce fulfillment require 8-10 ft aisle widths, 20-40+ ft lift heights, and 1.6-2.0 t capacity on smooth indoor floors; counterbalanced forklifts still win outdoor and dock work.
For retail distribution centers running 50 to 120 trucks per day, hydraulic dock levelers rated 25,000 to 45,000 lb dynamic load are the default 2026 specification; mechanical and edge-of-dock units suit only sub-30 cycle/day operations.
For port logistics, specify a hydraulic dock leveler with a working load limit of 8 to 10 tonnes (extendable to 12 to 25 tonnes for heavy industrial use), 2000 x 2500 mm platform, 400V three-phase supply, and IP54 controls. Match type to duty cycle, ambient temperature, and truck-height variance bef
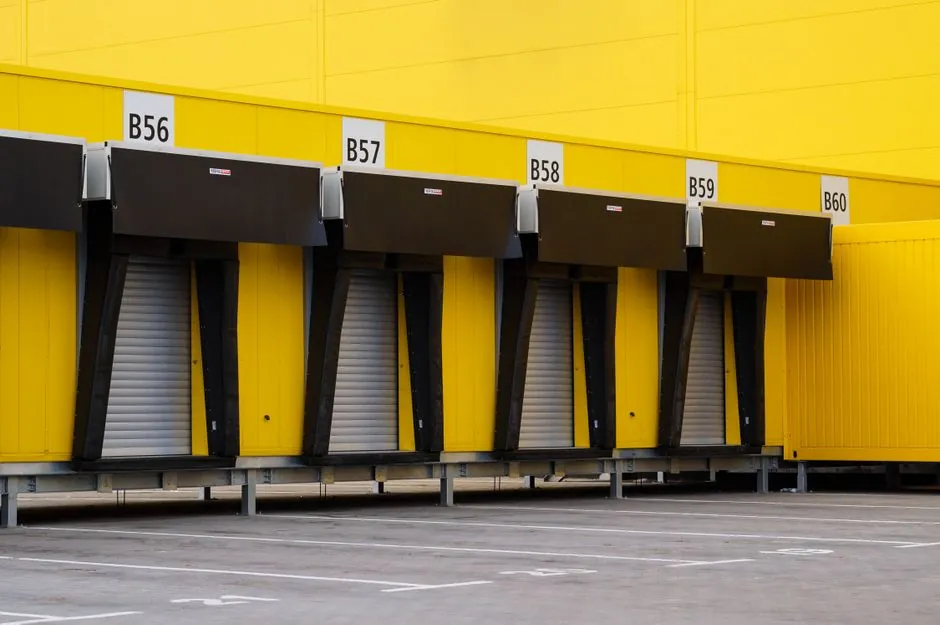
For apparel distribution, hydraulic dock levelers rated 25,000-35,000 lb dynamic capacity with 6-7 ft lips fit high-cycle receiving; vertical-storing models suit mixed-trailer fleets. Apparel DCs running 8+ truck turns per bay per shift should default to hydraulic, not mechanical, based on 2026 dock
Chemical shipping requires dock levelers built around corrosion resistance, spill containment, and DOT hazmat compatibility, not the standard pallet-rated 6–15 t units used in general logistics. Hydraulic models with ±250–300 mm travel, 50-cycle pre-shipment stress testing, and chemical-rated deck f
For automotive parts logistics, hydraulic dock levelers rated 35,000–150,000 lb with 8 mm anti-slip plate, 16 mm lip, and 120 bar hydraulic pressure are the dominant spec. Mechanical and air-powered units fit only low-cycle, budget-driven docks.
Pharmaceutical-grade dock leveler selection in 2026 hinges on three decisions: stainless or galvanized finish, hydraulic actuation with a velocity fuse, and a sealed pit package (PitMaster-style or brush/vinyl seals) to keep wash-down water and pests out of the GDP envelope.
Vertical and telescopic hydraulic dock levelers with ±250–300 mm travel and 6–15 t capacity are the dominant picks for cold chain bays in 2026, where every second of door-open time drives refrigeration load and HACCP/GDP exposure.
Hydraulic dock levelers are the default for e-commerce fulfillment centers, with push-button operation, ~12 inches of vertical adjustment, and capacities suited to high trailer turnover. E-commerce sites should match leveler type to daily cycle count, with edge-of-dock units reserved for low-volume
Retail distribution platform trolley selection hinges on matching 150-800 kg load ratings to cart SKU mix, PVC vs steel decks, and 5-8 in caster spec. Use 20-30% capacity headroom over average load. 300-500 lb dollies suit parcel hubs; 600-800 lb units serve appliance back-of-house.
Port-logistics buyers should pick a platform trolley by deck load, wheel diameter, and braking class matched to ISO container yard duty, not by generic warehouse ratings. For quayside and CFS work, 500–1000 kg decks, 200 mm polyureth
For apparel distribution, pick a platform trolley rated 20–30% above the heaviest typical carton, with a 900×600mm or 1000×600mm deck, fixed+swivel casters, and PU or rubber wheels; expect ₹3,000–₹6,500 in India and $80–$300 from Chinese OEM factories.
For electronics handling, specify an ESD-safe PVC platform trolley in the 150-300 kg class with 2-fixed/2-swivel castors and a conductive deck, sized to the largest PCB magazine.
Platform trolleys for chemical shipping should be specified as 316L or hot-dip galvanized steel with 150-300 kg load ratings, polyurethane or nylon wheels, and foldable frames, avoiding aluminium in chloride or acid service.
Platform trolleys for automotive parts logistics run from 45 kg light-duty flatbeds to 680 kg industrial heavy-duty carts, with wheel type (pneumatic, solid, flat-free) and castor layout (2-fixed-2-swivel vs all-swivel) doing more to determine uptime than deck material. Specify by load band, deck si
Stainless steel platform trolleys for pharmaceutical distribution are specified in SS 316L, mirror-polished to Ra < 0.4µm, with EN 10204 3.1 certification and crevice-free welds per June 2026 manufacturer data. Floor capacities range 150-1000kg, and finish grade plus castor selection drive 30-40% pr
For food and beverage plants, a platform trolley should be specified around hygienic finish (304/316 stainless), washdown rating (IP65 to IP69K where jet-cleaned), wheel diameter, load class, and deck material, then matched to a floor-scale or washdown scale where tare-in/cross-check is required. Wo
Platform trolley selection for cold chain logistics hinges on stainless or galvanized frames, 150–500 kg load ratings, polyurethane wheels rated to −30 °C, and hygienic finishes; motorized 500 kg+ sensor-equipped units are gaining ground for reefer docks and blast-freezer transfers per 2026 supplier
Manual pallet jacks in the 2,000–2,500 kg load range remain the default spec for retail backrooms and store-level distribution in 2026, priced at roughly $300–$700 new. They outperform electric models on cost, aisle manoeuvrability, and training burden, but cap out on throughput and operator strain.
Manual pallet jacks rated 2,500-3,000 kg are the practical default for air-cargo warehouse tarmacs, where ULD dwell stays under 24-48 hours and short-distance moves dominate. Spec the 3,000 kg class only when individual palletized loads regularly exceed 2,500 kg, otherwise the 2,500 kg truck cuts op
Manual pallet jacks remain the lowest-cost, lowest-training option for short-distance warehouse transport, with typical 4,000–5,500 lb capacity and a 5–7 year service life. For automated and high-throughput facilities, electric walkies reach 8,000 lb at 2.5 mph, and AGV pallet trucks deliver 20–30%
Manual pallet jacks rated 4,400 to 5,500 lb cover roughly 80% of apparel-pallet loads on a standard GMA pallet, making them the default pick for apparel DC receiving and floor-level put-away. A 27" x 48" fork, 3.0 to 3.5 inch lowered height, and polyurethane wheels are the three spec checks that mat
Manual pallet jacks rated 4,000-5,500 lb dominate electronics-handling aisles because ESD-safe nylon wheels, 2,000-2,500 mm turning radius, and a manual hydraulic pump let operators move 1-3 pallets per shift without OSHA Class III certification, unlike electric units.
For automotive parts logistics, select a 2,500 kg-rated manual pallet jack with 685 mm fork width and polyurethane wheels on sealed concrete, and shift to electric walkie or rough-terrain jacks once trip distance exceeds 30–40 m or floor quality drops.
Carton erecting machine prices in mid-2026 span roughly USD 3,000 for a basic L800-A hamburger/lunch-box former to USD 30,000+ for an automatic 180 cpm PLC line, with automation level, output speed, and material handling driving the largest cost gaps between Chinese OEM quotes.
Manual pallet jacks remain the right pick for short-range e-commerce staging when daily travel stays under ~50 m, loads sit in the 1–2.5 t range, and aisle width is non-constrained. They lose to electric pallet trucks once travel distance, shift length, or operator-fatigue data start climbing past 2
For retail distribution backrooms, a 1.0-1.5 tonne electric pallet stacker with 1600-3000 mm lift and a 800-1000 mm straddle footprint fits 2.4-2.8 m aisles, while 2.5-tonne manual stackers cover low-rise shelf restocking. Selection hinges on pallet type, daily throughput, and aisle width, not headl
For air-cargo pallet stacker selection, prioritize electric or semi-electric straddle units rated 600-2000 kg with a matched aisle width, and pair them with paper or composite pallets to cut air-freight tare weight while maintaining stack height limits for ULD compatibility.
Port pallet stacker selection hinges on four hard numbers: rated load 1200-1600 kg for new Li-Ion walk-behind high-lift trucks, aisle width, lift height, and surface grade. Match these against the dock-to-stacking route before choosing walk-behind, platform, or ride-on formats.
Pallet stacker selection hinges on five concrete spec gates: load capacity 600-2500 kg, lift height 1.6-5.5 m, aisle width, pallet type compatibility, and manual vs electric drive. Match these to throughput, then decide between rider stacker, AGV stacker, or pallet shuttle for high-density lanes.
For apparel distribution, an electric walkie pallet stacker in the 1500–2000 kg capacity band with 3000–4500 mm two-stage duplex mast typically fits standard EUR/ISO pallets in 1600–1800 mm aisles; specify lithium-ion power, anti-tip devices, and load backrests for delicate textile loads.
For electronics handling, electric pallet stackers in the 1.5-ton class with narrow-aisle straddle geometry, ESD-safe wheels, and lithium battery power cover most SMT/PCBA warehouse tasks; pure manufacturing on heavy reels should move up to the 2-ton class.
For automotive parts logistics, a 2-ton class electric pallet stacker with a stand-on platform, AC drive motor, and lithium battery is the dominant specification. Selection hinges on load class, lift height, aisle geometry, and whether the unit is being used for line-side delivery or pallet racking.
Pharmaceutical distribution sites should pick pallet stackers around four axes: cleanroom-friendly power vs manual, 1,200–3,000 kg payload band, lift height 1.6–5.5 m, and WMS/MES integration. Match the right class to lot size, GMP zoning, and throughput.
For food and beverage palletizing, an electric walkie stacker rated 2,200-3,500 lb at 24-36V typically fits ambient, chilled and frozen zones when the model is cold-spec verified, the floor is dry, and cleaning is washdown-safe. Semi-electric units suit low-volume rooms.
Cold-chain pallet stackers must combine low-temperature-rated hydraulics, batteries, and steel coatings with 1.5–3.0 kW electric drives and 1.6–2.5 ton capacities to survive condensation and sub-zero duty in refrigerated and frozen warehouses.
For e-commerce fulfillment in 2026, pick a walkie or rider pallet stacker rated 1,500-2,000 kg with electric lift, 3.0-5.4 m mast, and 2.4-2.8 m aisle footprint; bypass manual stackers and reach trucks for true unit-pick operations.
For retail distribution backrooms and supermarket replenishment, a low-profile electric pallet truck with 3,000-4,500 lb capacity on 27 in forks, paired with a manual jack for occasional moves, is the spec sweet spot as of 2026-08-20.
For air-cargo terminal pallet handling, electric pallet trucks in the 1,500–3,500 kg capacity class (including heavy-duty 6,000 lb / ~2,720 kg rental units) are the practical spec window, paired with a forklift where vertical lift is required. Selection hinges on ULD-compatible dimensions, battery r
Electric pallet trucks for port logistics typically range from $2,000 to $8,000 with 3,000-6,000 lb capacity, but port duty cycles demand lithium-ion 24V/48V power, IP-rated chassis, and matched BMS/charger platforms rather than entry-level warehouse units. Operators must prioritize duty-cycle mappi
Electric pallet trucks now hold roughly 42% of the global pallet jack market, with battery-powered walkie and rider models in the 1500–3500 kg range dominating distribution-center fleets. Selection in 2026 hinges on duty cycle, battery chemistry, and aisle width, not sticker price.
For apparel distribution centers, electric pallet trucks in the 3,300 lb (1,500 kg) class with 27 in x 48 in forks and 4.5 to 7.8 in lift height fit standard GMA floor-load apparel pallets; stainless-steel builds suit only wash-down or food-grade zones, not general picking aisles.
For automotive parts logistics, electric pallet trucks in the 3,000–8,000 lb class with 54-inch turning radius and 3.4–6.1 mph travel cover most line-side and cross-dock moves, while heavy-duty 6,000–30,000 lb walkie units handle stamping dies and engine blocks. Specify capacity, fork size, turning
For pharmaceutical distribution, spec an electric pallet truck in the 1500–3500 kg capacity band with stainless or corrosion-resistant hygienic construction, lithium-ion power, and pallet-jack compatibility for EUR 1200×1000 mm or CHEP 1219×1016 mm loads.
Electric pallet trucks for food and beverage typically span 3,000 to 8,000 lb capacity, with food-grade builds adding stainless hardware, sealed electronics, and IP-rated washdown enclosures for cold room and sanitation duty.
Electric pallet trucks for cold chain logistics need low-temperature-rated batteries (Li-ion or cold-room lead-acid), galvanized or stainless frames, food-grade lubricants, and capacity de-rating near 0°C. Standard 24V/48V walkie units rated 3,000–8,000 lb cover most cold storage pallet moves, with
Electric pallet trucks in the 1.5–2.0 ton class dominate e-commerce fulfillment procurement, with battery-powered walkie models delivering 140–180% of manual pallet jack productivity on long travel runs. Select on load, travel distance, aisle width, battery chemistry, and duty cycle rather than stic
AS/RS systems for air cargo terminals should be selected on Cargo Dwell Time KPIs and pallet-throughput targets, not equipment counts: McKinsey-cited data shows automated warehouses cut OPEX ~20% and lift throughput 15-20%, and H2 2026 air freight rates are projected 5-15% higher per Xeneta, making
AS/RS selection for warehouse automation hinges on matching unit-load, mini-load, shuttle, and vertical lift module architectures to SKU profile, throughput, and ceiling height, with crane and shuttle hybrids favored for mixed-pallet and tote operations above 6 m clearances.
For pharmaceutical distribution, mini-load AS/RS with goods-to-person stations and integrated vision picking now dominate greenfield builds, while unit-load cranes suit bulk API pallets; key 2026 selection criteria are throughput per aisle, validated cold-chain integration, and WMS/GxP auditability.
Specifying an AS/RS for food and beverage hinges on temperature-rated storage, hygienic materials, and SKU profile: pallet-stack cranes suit ambient/case picking, unit-load miniload serves slow-movers, and shuttle-based totes handle high-rotation SKUs under 25 kg.
Conveyor sorting line selection for retail distribution is a spec-first exercise: throughput, item profile, destination count, accumulation behaviour and floor footprint drive the choice between belt, roller, MDR, zero-pressure accumulation, tilt-tray and cross-belt sorters. For stores under 50, gra
Selecting a conveyor sorting line for air cargo starts with matching throughput, ULD/pallet footprint and dangerous-goods segregation to the integrator's floor. Belt vs roller vs cross-belt sorter, bar-code/RFID read rate and CEIV-Pharma zoning decide the line layout before any brand is named.
Port-logistics conveyor sorting lines are built from cross-belt, tilt-tray, sliding-shoe, and roller-bed modules running 1.5-6.0 m/s; selection should be driven by parcel profile, throughput, and dwell, not brand. Ro-Ro ports should benchmark vehicle processing, dwell, and rail/truck access before c
Specifying a conveyor sorting line for warehouse automation in 2026 means matching sortation type (wheel, narrow-belt, cross-belt, sliding shoe) to SKU profile, throughput, and WMS/WCS integration. Belt-driven live roller and zero-pressure accumulation remain the workhorses for case handling; vision
For electronics handling, a spec-first conveyor sorting line pairs ESD-safe belt materials (static-dissipative PU or modular PP) with cross-belt or narrow-belt sorters at 30-120 units/min throughput, picking by width/length/weight or vision. Match sorter type, belt class, and frame grounding to your
For chemical shipping conveyor sorting, specify belt or roller sorters in 304/316 stainless with sealed bearings, NEMA 4X panels, and ATEX/IECEx-rated zones. Match sorter class (cross-belt, slide, pop-up wheel) to carton vs drum, ESD/ATEX zone, and target sort rate up to 200/min.
Pharmaceutical distribution conveyor sorting lines must pair hygienic construction (typically 304/316 stainless steel, tool-free disassembly, FDA/EU 10/2011 contact surfaces) with throughput matched to carton weight. For orders below 7,500 units/h under 50 kg, a high-speed belt or roller sorter such
Food and beverage conveyor sorting lines are selected on three concrete axes: hygienic construction (304/316 stainless steel, IP65+ washdown, food-grade belt material), throughput range (typically 30-180 packs/minute), and integration with VFFS or thermoformer infeed. ABB drive packages and Jenton A
Air cargo sorting systems must be selected around unit load device (ULD) footprint, throughput per hour, and dual-mode screening compatibility, not by brand. Use this four-criteria filter: ULD mix vs sortation lane geometry, hourly piece count, screening integration (CT/EDS), and WCS/M&E interfa
Port-logistics sorting systems are typically cross-belt or tilt-tray units rated 6,000-12,000 boxes/hour, selected by parcel mix, footprint and integrator fit. For 2026 port bids, modular diverter-based sorters from Flowsort and similar vendors are displacing fixed roller sorters on greenfield build
Automotive-parts sorting lines pair swivel-wheel diverters (100-3,000 pcs/hr per chute) with DWS scan-weigh-dimension units (3072x2048 imaging, 10g-60kg scale) on conveyor or AGV feeds; choose by SKU mix, part weight, traceability bar.
Central-fill pharmacies increasingly evaluate conveyor-based sorting systems against AGV sorting systems on throughput, cycle time, and AGV-count sensitivity, with KPI-driven two-stage assignment models documented in 2024. Selection is for high-SKU, expiry-controlled operations requiring GMP-aligned
Sorting systems for food and beverage must be selected against EHEDG hygienic-design, HACCP, and FDA/EU 1935/2004 contact-surface rules, then matched to the contamination risk of the product (dairy, bakery, beverage, confectionery). Optical + metal-detection hybrid sorters are the practical default
Cold chain sorting system selection hinges on three gates: product temperature band (-25°C to +15°C typical), throughput (parcels/hour per lane), and dwell time at the sorter. Cross-belt sorters lead for high-mix pharma and seafood, while shoe-sliding or tilt-tray sorters fit chilled grocery at lowe
Sorting system selection for e-commerce fulfillment hinges on matching throughput tier (500-3,000, 3,000-15,000, 15,000+ parcels/hr) to order profile, SKU mix, and peak ratio. Cross-belt, sliding-shoe, tilt-tray, and shoe-belt sorters each lock in different accuracy and SKU-shape envelopes.
For air-cargo operations, a Vertical Lift Module (VLM) cuts storage footprint up to 90%, integrates with WMS/ERP, and serves as a closed-loop buffer for ULD components, engines, and high-value parts. Spec selection hinges on tray payload (typically 500-1,000 kg), unit height, delivery type, and dual
Port-logistics VLM selection hinges on marine-grade enclosure (IP54–IP65, salt-fog per IEC 60068-2-52), tray payload ≥1,000 kg, and dual-level delivery to keep dwell time below 30 s. The VLM segment hit US$950.19 Mn in 2024 with a 9.7% CAGR through 2031. Pick stainless/epoxy-coated columns, dua
Vertical lift modules (VLMs) are enclosed tray-handling storage systems for warehouse automation, with units up to 16,100 mm tall, single-tray payloads reaching 990 kg, and throughput near 120 trays per hour. Selection hinges on payload, throughput, bay layout, and WMS integration rather than price.
Automotive parts logistics operators selecting a Vertical Lift Module in 2026 should size on footprint reclaim (typically up to 90% of original inventory relocated into one unit), dual-level delivery, and WMS/ERP integration, with the automotive segment holding 32% of the global VLM market in 2024.
Vertical lift modules (VLMs) for food and beverage plants typically need stainless or coated trays, sealed enclosures, dual-level delivery bays, and WMS/ERP integration, with the global VLM market projected to grow from US$950.19M in 2024 to US$1,766.08M by 2031 at a 9.7% CAGR.
Shuttle-based storage and retrieval systems (SB-SRS) split into 2-way pallet shuttles, 4-way shuttles, bin/tote shuttles, and OSR-style goods-to-person units. Selection turns on SKU profile, throughput, fire code, and cold-chain duty rather than raw throughput claims. Spec gates: 1.0–1.5 t/unit pall
Shuttle systems for automotive parts logistics fall into two practical families: physical racking shuttles, sized by payload, lift height, and aisle depth, and software shuttles that run dealer-side parts delivery. Spec gates split on part size, throughput, and integration with MMOG/LE supply audits
Shuttle systems for pharmaceutical distribution are selected by throughput-per-aisle, ambient control, and serialization compliance, with multi-shuttle topologies delivering 100%+ throughput gain over single-shuttle designs in IIE modelling.
Shuttle system selection for food and beverage warehousing hinges on hygienic-design rails, stainless or polymer-clad carriers, IP65+ shuttle electronics, and temperature-zone segregation across cold, dry, and ambient storage. ISO 22000 and HACCP-aligned intralogistics with EHEDG-cleanable surfaces
Pallet shuttle selection for cold-chain logistics in 2026 hinges on temperature rating, storage depth, and redundancy architecture, not headline throughput. Two-way shuttles fit deep-lane single-direction frozen storage down to -40°C, while four-way shuttles serve multi-level mixed-SKU chilled opera
Shuttle systems built around each-to-pick storage, decentralized drive control, and PC-based soft PLC deliver 25% lower hardware cost in e-commerce DCs, with viability gated above 500–1,000 SKUs and 30,000+ orders/day per shuttle cluster.
Retail-distribution AMR selection in 2026 hinges on payload class (up to 1500 kg), navigation stack, and fleet-manager interoperability, with the global AMR market projected to reach $14.40Bn by 2030 at a 21.4% CAGR. Goods-to-person units, autonomous inventory robots, and self-driving forklifts

Autonomous Mobile Robots (AMRs) for air cargo terminals must be specified against payload class (50-1500 kg), navigation method (LiDAR SLAM vs. depth-camera), battery cycle life, and FAA/IATA ULD compatibility. KUKA's 2026 white paper frames AMR selection around these four gates for manufacturing-sc
Port-logistics AMR selection hinges on payload class (300–600 kg), IP rating, navigation stack, and ROI payback, with suspended chassis designs validated up to 500 kg load. Yard-grade units integrate LDS plus depth-camera fusion, 8-hour runtime, and Wi-Fi/LTE fleet control.

For apparel distribution in 2026, AMRs with QR-code floor referencing and 30-300 kg payloads dominate tote and hanger-cart flows, while Visual SLAM units fit retrofits without floor marking. Pick by SKU mix, aisle width, and ceiling clearance rather than brand.

AMR selection for electronics handling hinges on four spec gates: floor-load rating, ESD-safe chassis, 2D LiDAR + vision sensor fusion, and payload class of 150-1900 kg. OTTO 100, 600, 1200, 1500, and Lifter are cited payload options for 2026 fabs.

AMRs for chemical shipping must be selected on a 1.0–2.5 m/s speed band, ATEX/IECEx Zone 1 compatibility, and stainless or chemical-resistant top modules, not on raw payload alone. For tanker, drum, and IBC moves in classified areas, stainless-deck AMRs with intrinsically safe add-ons outperform car

For automotive parts logistics, AMR fleets in 2026 are selected on four gates: payload class 100-1500 kg matched to SKU bin weight, VDA 5050 fleet interoperability, mixed-traffic safety (ISO 3691-4 PLd Cat 3), and aisle/turning radius under 1.2 m. Pick the wrong gate and you buy the wrong robot.

AMR selection for pharmaceutical distribution hinges on ISO Class cleanroom compatibility, GMP-grade stainless or sealed payloads, validated SLAM under fluorescent lighting, and audit-ready fleet software. Avoid general factory AMRs lacking particulate control and 21 CFR Part 11 traceability.
Food and beverage AMR selection hinges on stainless or IP65-rated chassis, food-grade lubricants, SLAM navigation tolerant of wet floors, and payload matched to pallet or rack loads. Stainless steel construction and NSF/3A washdown readiness are the dominant spec gates for 2026 deployments.

AMR selection for cold chain logistics in 2026 hinges on five gates: payload tier, temperature-rated battery and lubricant, navigation modality, fleet control software, and validated cold-storage insulation. AMRs are not suited for sub -25 °C blast freezing or open-door yard handoffs without a shelt

AMRs outperform AGVs in e-commerce fulfillment because onboard perception and SLAM let them reroute around dynamic obstacles without floor wiring. Selection hinges on payload 10–1500 kg, fleet size, and aisle width, with collaborative-sorting limits around 1.5 m/s near humans per MARS guidance.
Retail distribution pallet rack selection turns on SKU count, throughput, and floor footprint. Teardrop selective rack is the default for 100% SKU access, with 33,000 lb frame capacity and ANSI MH16.1:2021 governing the spec.
Air-cargo pallet rack selection is driven by air-freight ULD compatibility, payload bands of 1000-4000 kg/shelf (Q235 cold-rolled steel), and IATA air-pallet footprints. UPS, Lufthansa Cargo, and Finnair publish pallet/ container guidance that the rack spec must trace back to.

Port-logistics pallet rack selection pivots on load class (typically 8,000–12,000 kg/frame), corrosion protection for marine air, and compatibility with ISO container pallet footprints. Choose hot-dip galvanized or pre-galvanized steel for berth-side zones, selective teardrop for mixed SKUs, and dri
Selective, drive-in, cantilever, push-back, and radio-shuttle pallet rack each map to a different SKU velocity, aisle width, and forklift class; specifying the wrong family typically costs 20-40% of usable cube and is the leading cause of racking-related downtime. Match rack family to pallet size, t

Teardrop selective pallet rack is the default pick for apparel distribution: 48-hour ship teardrop frames/beams, 10%+ online discounts, and selective slots dominate the 2026 mid-tier DC market. Apparel volumes are light, so 2,500-3,500 lb per-level beam capacity and wire-decked shelves beat drive-in
For electronics handling, choose a roll-formed selective pallet rack with ESD-safe plastic pallets, individual lane FIFO, and zinc-plated or painted frames rated 8,000-12,000 lb per beam pair. Avoid drive-in or push-back for mixed-SKU electronics work.
Chemical-shipping pallet rack selection hinges on capacity, deck drainage, frame finish, and code compliance, with roll-formed selective racks dominating drum and tote storage at 20,000-30,000 lb bay loads.
Automotive parts logistics favors selective pallet racking for mixed SKUs and drive-in or push-back for high-density batched lines, with galvanized or powder-coated finishes mandatory for humid zones. Spec gates span 800–4,000 kg UDL per beam pair, 2,400–11,000 mm bay height, and FEM/EN 15635 or RMI

Pharma distribution pallet rack selection hinges on four gated decisions: steel grade and surface finish for cleanroom adjacency, beam capacity at the actual unit load (not catalog max), selective vs drive-in density, and seismic/anchoring compliance per local code. Teardrop selective racks at 4,000

Cold chain pallet rack selection balances steel grade, finish, temperature rating, and rack geometry against SKU velocity. Drive-in and shuttle racks raise density 40-60% versus selective layouts but trade away FIFO; galvanized or powder-coated frames are specified down to roughly -25°C ambient serv
Pallet rack selection for e-commerce fulfillment hinges on three gates: SKU profile, throughput model, and seismic/fire code. Selective, drive-in, pallet-flow, push-back, and cantilever each fit a distinct velocity-versus-density trade-off, with capacities typically 8,000–40,000 lb per bay.

Retail-distribution AGV selection in 2026 hinges on four hard gates: payload class (sub-500 kg shelf runners vs 1000–3500 kg pallet units), lane-discipline vs free-navigation topology, total deployment cost not unit price, and integration with WMS/PLC power cabinets on site.

Air-cargo AGV fleets are being specified for 1–6 ton ULD and pallet moves, with selection gated on payload, lift height, navigation type, and ATEX/IECEx zone rating. Lufthansa Cargo serves 350+ stations across 100 countries; Amazon Air Cargo operates 100+ aircraft on 250+ daily flights, anchoring th

For port logistics in 2026, AGV selection should be anchored on payload class (1,000-2,500 kg for container handling, sub-500 kg for trailer spotting), outdoor-rated navigation (laser SLAM or GNSS+RTK), and IP65+ enclosure protection. The global AGV market reached USD 6.51 billion in 2026 and is for
AGV selection for electronics handling pivots on payload (50–1500 kg), navigation type (magnetic tape vs multi-line LiDAR 3D SLAM), and ESD-safe chassis. Match vehicle class to PCBA tote weight, aisle width, and cleanroom class, and validate the safety stack (LiDAR zones, anti-collision strips, ISO

Selecting AGV robots for pharmaceutical distribution hinges on three gate decisions: GxP-cleanable chassis with stainless or sealed IP54+ bodies, two-stage package assignment software that pairs upstream induction flow with sortation slots, and a 1-3 year ROI target backed by 30%+ throughput gains.
AGV robot selection for food and beverage lines hinges on hygienic design (IP ratings, food-grade materials, EHEDG zone concept), payload vs. tugger mass, and cleanability under washdown. Match AGV class (unit-load vs. tugger vs. mobile manipulator) to throughput, aisle width, and ambient temperatur

Port-logistics stacker cranes are specified by aisle width, lift height, payload class, and AS/RS integration rather than crane type alone. Selection hinges on container/pallet mix, throughput duty, and seismic/wind class, with rail-mounted units dominating high-density terminal blocks.
Stacker crane selection for warehouse automation hinges on pallet footprint, aisle depth, throughput cycle time, and WMS/WCS integration. Standard 1200x1200x1200 mm pallets, single/double-deep and straight/fork fork types are common ASRS configurations.
For chemical shipping warehouses storing 200 L drums, IBCs, and palletized reagent containers, a stacker crane must be selected to ATEX/IECEx Zone 1 or Zone 2 with stainless or epoxy mast, 1000-1500 kg payload class, and double-deep or single-deep aisle layout matched to drum dimensions.

Stacker cranes for automotive parts warehouses are specified by load unit (pallet or box), aisle width, and storage height, with trilateral pallet cranes fitting existing racking up to 15 m and Miniload box cranes reaching 20 m in 800 mm aisles.

Stacker cranes for e-commerce fulfillment are unit-load AS/RS machines on floor or top rails, with steel-column masts, steel-wheeled bogies, and telescopic forks; Mitsubishi Electric's logistics solution page documents cycle-time reduction, safety, and inbound/outbound flow gains for these systems [

Vibrating conveyors serve retail distribution when parcel and packaged-goods flows need gentle, sanitary, low-noise transport with trough widths from 300-1200 mm. Electromagnetic drives fit light duty; eccentric or dual-motor designs handle heavier cartons and totes up to around 50 kg/m.

Vibrating conveyors in air-cargo terminals are sized by unit-load-device (ULD) footprint, throughput per hour, and noise ceiling rather than by bulk-density alone; selection rules from Finnair, EVA Air, and Polar Air Cargo operations converge on 1.5–3.0 kW drives, stainless contact surfaces for phar

Vibrating conveyors earn warehouse-automation slots where they must move small, dry, granular or unit-packaged loads on a compact footprint without oil-lubricated drive parts contaminating the line. Selection hinges on four spec numbers: trough width, amplitude (typically 3–12 mm), vibration frequen

Vibrating conveyors for automotive parts logistics fit small, dry, free-flowing components (fasteners, clips, stampings) on trough widths 200-600 mm and amplitudes 2-8 mm, with linear or circular drive modes selected by part fragility and feed rate. They are not specified for oily, hot (>150 deg C)
Food-grade vibrating conveyors for bakery, snack, and frozen-food lines are typically specified as 304/316L stainless troughs, sanitary designs meeting 3-A or EHEDG hygiene practice, and amplitudes of 4–8 mm at 50/60 Hz, with electromagnetic drives preferred for low-maintenance sanitary service and
Vibrating conveyors are not a mainstream pick for e-commerce parcel handling: they excel at moving bulk, free-flowing, or unit-packaged material on a fixed trough, while most DC sortation still rides on belt, chain, and overhead lines. Use a vibrating conveyor only when the SKU profile is uniform, d

Pneumatic conveying for cold chain logistics centres on dilute-phase vacuum or pull-push systems running 3000-8000 fpm, sized below 10 tons/hr with positive-displacement blowers and air/material ratios above 2.0, chosen for sealed, dust-free transfer of starch, sugar, dry milk, salt and plastic pell
Vertical lift modules (VLMs) reclaim 75-90% of floor area in parts warehouses and typically pay back inside 18-36 months; 2026 buying hinges on tray footprint, payload, height, WMS integration, and AMR coupling.
Vacuum packaging machines evacuate air from a chamber or bag before heat-sealing, while capping & sealing machines close a container with a cap or film seal. Use a vacuum packer for shelf-life and oxidation control; use a capper/sealer for rigid container closure, torque control, and high-speed bott

AGV robots cut labour in fixed-path material handling, with three mainstream guidance modes—magnetic tape, laser and UHF RFID—each trading cost against layout flexibility and accuracy. They are not a fit for unstructured sites, very long outdoor hauls, or high-mix low-volume flows.

Shrink wrapping machines deliver 10-120 packs/min throughput, 5-7 year service life, and film-only or pad-plus-film pack formats, but carry higher film cost per pack, energy draw from heated shrink tunnels, and limited suitability for very tall or unstable loads. Specification, not brand, drives ROI

Pneumatic conveying system selection hinges on four decisions: dilute vs dense phase, positive-pressure vs vacuum, batch vs continuous duty, and material-air compatibility. The global market is forecast to reach USD 48.36 billion by 2030 at a 5.8% CAGR (2023-2030), driven by pharmaceutical, food and
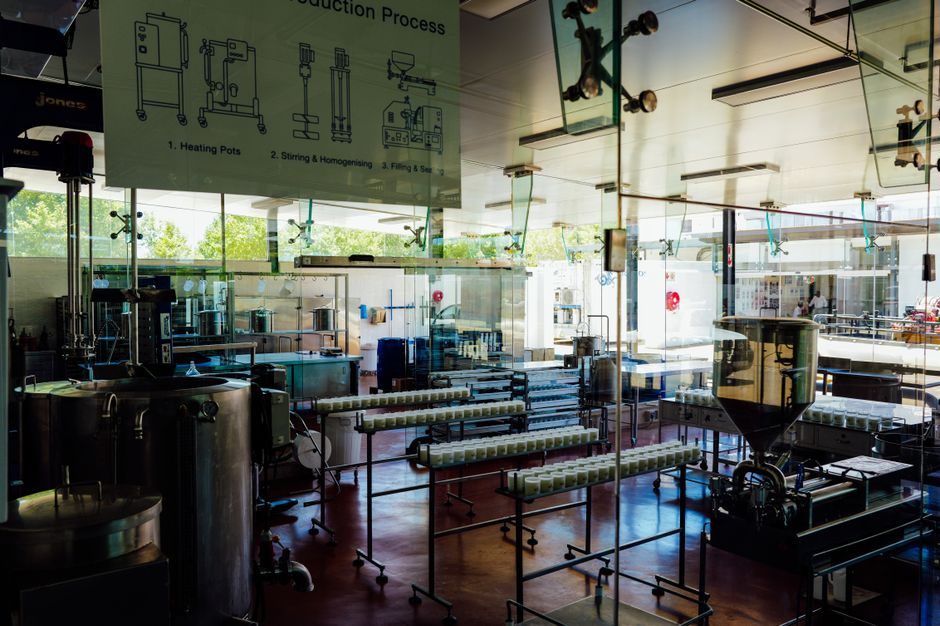
Overhead conveyors for food and beverage are selected on four spec gates: 304/316 stainless construction, USDA/3-A/BISSC hygienic compliance, 20-200 FPM line speed, and enclosed-track guarding. Enclosed-track is now standard for high-throughput F&B lines per IQS Directory (2026-06-16).

Truck scale TCO spans a 20+ year lifecycle where purchase price is roughly 30-50% of lifetime spend, with foundation, load cells, calibration and downtime driving the balance. Buy on reliability and service, not on sticker.

Wrapping machines divide into stretch, shrink, wrap-around sleeve, banding, and overwrapping classes, each defined by film type, sealing method, and throughput. Selection turns on product geometry, film width, output in cycles/min, and line integration rather than brand.
For e-commerce fulfillment, dilute-phase vacuum or pressure pneumatic conveying suits lightweight dry goods up to 200 lb/ft³, while dense-phase systems handle fragile pellets at 2,500–6,000 fpm; selection hinges on material density, throughput, and contamination control rather than conveyor footprin

Centrifugal discharge bucket elevators rated 200 to 1,300 BPH with HDPE or urethane buckets on a single-trunk casing fit retail-distribution duties where product damage matters more than peak tonnage. Selection hinges on material density, lump size, moisture, discharge height, and whether the EASY D

Air-cargo terminal bucket elevator selection hinges on throughput, lift height, bucket profile, and ignition-risk control rather than bulk-mining capacity. Specify centrifugal-discharge units in the 80 to 700 m³/h range, with HARDOX or PEHD wear liners and ATEX-rated belt-speed monitoring, for parce

Port-logistics bucket elevators for grain, cement, fertilizer and mineral bulk are selected on eight data points: capacity in BPH or m³/h, lift height, bulk density, lump size, moisture, temperature, dust/explosion class, and duty hours. Centrifugal discharge units fit free-flowing dry bulk at high
Bucket elevators for warehouse automation are selected on seven spec gates: material bulk density, capacity in ft3/hr or BPH, lift height, lump size, temperature, moisture, and duty hours. Match centrifugal vs continuous discharge to throughput, then validate with belt/chain, bucket material, and dr
For apparel distribution, centrifugal bucket elevators with light-duty fabricated steel or aluminum buckets on PVC/polyester belting are the practical fit, sized around 500-3000 cu ft/h at 150-300 fpm for finished garments and cartons. Continuous-bucket or food-grade stainless units are specified on

Bucket elevators for electronics handling favor slow-speed continuous or positive-discharge designs with 304/316 stainless buckets, static dissipative belting, and sealed casings to prevent ESD, contamination, and chip migration. Capacities typically range from 20 to 500 BPH at low lift heights for

Bucket elevators used in chemical shipping require stainless or urethane construction, centrifugal or continuous discharge, and belt or chain media matched to the bulk density, corrosivity, and friability of the cargo. The dominant trade-off is 304 vs 316 stainless, with 316 specified where chloride

Bucket elevators for automotive parts logistics are typically specified as low-speed continuous or gentle-discharge units with 75-630 ft3/hr capacity, selected against a fixed 9-item data sheet covering material density, lump size, and lift height. Use a centrifugal unit only for free-flowing granul
Food and beverage bucket elevators must use 304/316 stainless contact parts, USDA/FDA-compliant polymers, wash-down-rated IP66 motors, and centrifugal discharge for free-flowing grains, sugar, salt, and milk powder at 50-100 m/h belt speed.

Cold chain bucket elevators need stainless or food-grade contact parts, low-friction slow-speed chains, enclosed dust-tight casings, and CIP/wash-down capability. Specify by material temperature, moisture, and BPH capacity before choosing centrifugal or continuous discharge.

E-commerce fulfillment bucket elevators are specified around five gates: parcel mass, hourly throughput, lift height, dimensional envelope, and food-grade or static-control material. Centrifugal designs dominate parcel hubs up to 4,000 parcels per hour; continuous-flow designs take over above that,
Overhead conveyors for port logistics typically use power-and-free or electrified monorail (EMS) configurations to handle unit loads up to 2,000 kg, chain pulls sized at 0.035 × total live load, and salt-spray rated components for marine exposure. The 2026 spec baseline centres on high-strength stee
Overhead conveyors maximize vertical warehouse space by suspending loads on ceiling tracks, with monorail, power-and-free, and enclosed-track variants selected by payload, accumulation, and routing needs. Power-and-free dual-track systems let carriers stop for processing while the chain continues, s

For apparel distribution centers, overhead conveyor selection turns on three numbers: unit load ≤30 kg per garment carrier, chain speed 1–30 m/min, and motor power as low as 0.37 kW for light-duty garment loops. Closed-track and power-and-free configurations dominate goods-on-hanger (GOH) flow, with

Overhead conveyors, particularly enclosed-track and power-and-free types, are the workhorse for automotive JIS lines because suspended transport preserves FIFO door, engine, and sub-assembly sequencing while freeing floor space. Selection hinges on per-carrier load, curve radius, paint-shop compatib

Overhead conveyors suit pharmaceutical distribution only when floor space is tight and loads can be hung or carted; 316/316L stainless under cGMP and FDA 21 CFR runs 10-120 FPM and outsources ground-floor traffic into ceiling airspace.

Overhead conveyors are specified for e-commerce fulfillment when floor space is constrained and items can be hung or carrier-mounted, freeing usable workspace and routing above active pick/pack zones. They pair with belt, MDR, and AGV lines rather than replacing them, with selection driven by load,
Wire mesh belt conveyors are a defensible pick for retail distribution only when open-mesh airflow, oil drainage, or washdown sanitation are real requirements; otherwise flat belt or modular plastic belts deliver lower cost and quieter operation.
Mesh belt conveyor selection for air cargo terminals hinges on five gates: belt weave type, stainless grade, width-to-bag ratio, drive duty, and ULD compatibility. T304 stainless balanced-weave mesh paired with 1.5–3.0 kW VFD drives covers 85% of narrow-body air-cargo cells.

Port-logistics mesh-belt conveyor selection hinges on belt weave, open area, drive pitch and edge reinforcement rather than brand. 316L stainless or balanced spiral weaves at 60% max open area suit bulk dry cargo; chain-driven edges handle 30 t/h+ throughput on dock unloaders.

Mesh belt conveyors for electronics handling are typically specified as 304 stainless steel balanced weave or polyester monofilament mesh, with edge rigidity, opening size, and tracking tolerance (≤3 mm roller misalignment) as the governing selection criteria.

Mesh belt conveyor selection for chemical shipping hinges on stainless-steel grade, mesh weave pattern, drive type, and belt-tensioner design. Specify 304/316 stainless steel with balanced-weave or chain-edge construction for corrosive cargo handling.
Mesh belt conveyors for automotive parts logistics typically use 304/316 stainless steel balanced spiral or flat-wire belts, with chain-driven variants rated −55 °C to 1150 °C. Selection hinges on part weight, oil exposure, and turn radius.

Mesh belt conveyors for pharmaceutical distribution require 304/316L stainless steel belts, FDA/EC1935-compliant materials, and cleanable weave patterns. Selection hinges on belt type, hygiene design, and load capacity. Avoid when abrasive or heavy bulk transfer is required.
Food-grade stainless steel 304/316 mesh belt conveyors are the default specification for washing, blanching, freezing, and baking lines operating between -40°C and 400°C, with belt pitch, edge profile, and drive direction chosen per process zone. Selection pivots on three engineering decisions: allo

AISI 304/316 spiral or flat-flex mesh belt conveyors running at 0.5-1.5 m/s are the baseline pick for cold chain zones between +2 °C and +8 °C; for freezing tunnels below -18 °C, chain-driven SS mesh with rod reinforcement is the only durable choice.
For e-commerce fulfillment, mesh belt conveyors split into metal flat-flex, PTFE-coated fabric, and chain-driven designs. Pick by carton weight, temperature, and washdown duty; SUS304 mesh serves cold storage, PTFE suits -70°C to +200°C zones, metal flat-flex handles heavy parcel lines.

Chain conveyors for apparel distribution must prioritize garment-friendly load geometry, low-noise operation under 75 dB(A), and modular line layout over the heavy-duty bulk ratings of cement or coal duty. Selection pivots on carton/soft-pack dimensions, sortation interface, and floor-load limits ra

Chain conveyors for chemical shipping must be specified to match load, corrosion class, and zoning: CMM-PHB's 6"S power-and-free line is a reference in rolling mills, while BFW-series chain conveyors target 1000 sets/yr capacity from Asian OEMs. Hengjiu's large conveyor chain spans auto, c

Chain conveyors for cold chain logistics are typically stainless-steel drag or slat-top variants with sealed bearings, sized for −25 °C to +8 °C pharmaceutical loads at 0.3–0.6 m/s, with selection driven by EU GDP and ISTA 7E thermal mapping. Specs must pair chain pitch, lubricant grade and cleanabi
Retail distribution screw conveyors are typically CEMA-standard 4- to 12-inch U-trough or shafted units sized for 50–500 lb/h flows of bagged goods, dry pet food, and granular product, with carbon-steel flights and quick-clean hanger bearings dominating the SKU set.
For warehouse automation, horizontal or shallow-incline screw conveyors sized to 30° max inclination (45° with engineered design) in carbon or stainless steel are the practical default when moving bagged dry bulk, grain or reclaim fines. Selection hinges on five numbers: bulk density, particle size,
Screw conveyors are engineered for bulk powders and solids, not for loose apparel — for garment distribution, specify a flexible screw/auger or tubular cable conveyor only when handling trimmings, off-cuts, or shredded fiber; standard inclined units cap at 30–45°.
Screw conveyors for electronics handling are typically specified as small-diameter (≤150 mm) stainless-steel tubular units running at 20–120 rpm, sized for sub-50 kg/h throughputs of wafer scrap, SMT trimmings, and connector cut-offs. Selection is governed by ESD-safe surface resistance (typically 1
Specifying a screw conveyor for chemical shipping hinges on material corrosion class, ATEX zone, temperature envelope, and angle of incline up to 45°. Carbon steel, stainless 304/316, and high-alloy options are all offered, with ATEX 2014/34/EU and the Pressure Equipment Directive as the binding Eur

Screw conveyors for automotive parts logistics are typically sized for short-haul, low-tonnage transfer of bulk and small-batch components, with selection driven by part geometry, contamination risk, and CEMA-standard component fit.

Food-grade screw conveyors specify 304/316 stainless contact parts, sanitary UHMW hanger bearings, and EHEDG/3-A cleaning access; the right pick depends on moisture, fat, and CIP regime.

For cold-chain logistics, spec a horizontal U-trough screw conveyor in 304/316 stainless with food-grade contact surfaces, insulated or jacketed trough for sub-zero duty, and a shafted (not shaftless) flighted screw sized for the product's bulk density and lump limit, per CEMA-aligned selection inpu

Screw conveyors are rarely the first pick for parcel e-fulfillment lines, where belt and roller conveyors dominate; they earn their place in the back-end where they meter free-flowing granulars, recyclables, and packaging waste at controlled rates per CEMA selection criteria.

Retail distribution roller conveyor selection hinges on four matching decisions: carton weight vs roller pitch, straight-run vs curved geometry, gravity vs powered drive, and CEMA/CEMA-class equivalent load rating. For typical 5-30 kg e-commerce cartons at throughputs under 1,500 cartons/hour, unpow

Roller conveyor selection for air-cargo terminals hinges on ULD-compatible roller diameter, drive type, and frame-load class, with galvanized steel and UHMWPE sleeves dominating 2026 OEM catalogues.
Roller conveyor selection for warehouse automation hinges on matching drive type, roller diameter, and load class to throughput and SKU profile. Powered roller lines run US$400–37,000 per set; decentralized geared-motor drives cut TCO at high variant counts.
Roller conveyors for apparel distribution centers are typically sized to 50 kg/unit load at 5-60 m/min belt or roller speed, with PVC or galvanized steel rollers on precision bearings for the carton and polybag lanes that dominate garment DC flow.

Electronics handling roller conveyor lines should default to 25 W 24 V DC motorized rollers on 50-60 mm pitch with 76 mm tube diameter, ESD-safe PU or galvanized steel tubes, and CEMA B-Series idler geometry, sized for ≤50 kg/m unit loads. For PCB or cleanroom-class flows, specify ISO Class 5 compat

Roller conveyors for chemical shipping typically use galvanized or SS304/SS316 tube rollers on hot-dip frames, sized to 50–250 kg/m load class per ANSI/CEMA 401-2003 and selected for drum-spill, pallet-drum and IBC tote duty in 2026 builds.
Roller conveyor selection for automotive parts logistics hinges on matching roller diameter (1.9"/2.5"/3.5"), drive type, and load class to part weight and routing geometry. Gravity, line-shaft, and motorized-roller (MDR) are the three main options, each with a distinct cost-vs-control trade-off.
Pharmaceutical roller conveyor selection hinges on stainless construction, cleanroom compatibility, and load rating: 1,500-4,500 kg pallet lines run at 12 m/min on S235JR frames, while carton lines need 24V ZPA accumulation with Interroll/Rulmeca rollers in cleanroom-rated finishes.
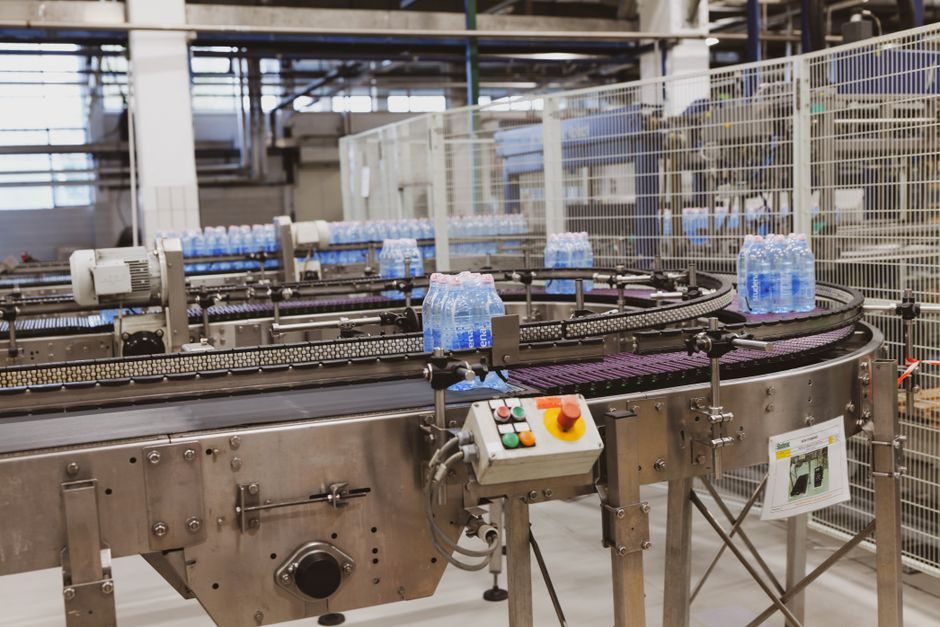
Roller conveyor selection for food and beverage hinges on three spec gates: sanitary materials (304/316 stainless or food-grade polymer rollers), washdown rating (IP65/IP66 minimum, IP69K for high-pressure cleaning), and a throughput band matched to the line — typically 1,000–5,000 kg/h for inspecti
Roller conveyors for cold chain logistics must combine stainless or zinc-plated steel construction, low-temperature-rated bearings, and food-grade lubricants to operate between -20°C and +60°C. For -25°C frozen zones, specify 304/316 stainless rollers with sealed-for-life bearings and ISO 9001-certi

Roller conveyor selection for e-commerce fulfillment hinges on matching roller diameter, pitch, drive type, and accumulation behaviour to parcel size, weight, and sortation throughput. Three decision axes — gravity vs powered, line-shaft vs motorised-roller (MDR), and zero-pressure-accumulation (ZPA
For retail distribution centers, belt conveyor selection hinges on carton size, throughput in cartons per minute, and incline angle; modular belt and telescopic boom units dominate 2026 short-line and dock-loading layouts, with light-duty modular conveyors typically rated to 100 kg and 0.1–0.5 m/s.

Belt conveyor selection for air-cargo terminals hinges on belt width, load per metre, incline angle, and ULD compatibility rather than throughput claims alone. Curved troughed and modular belts suit ULD transfer; flat endless belts suit parcel sortation under 50 kg/m.
For apparel distribution, specify a low-profile flat PVC or modular plastic belt conveyor running 0.3–0.8 m/s with 50 mm thermoplastic drive rollers, matched to garment weight, carton size, and sortation throughput targets.

For automotive parts logistics, belt conveyor selection hinges on payload band (≤40 kg, 600 kg, 2,000 kg), belt type, and accumulation duty; modular plastic and fabric belts dominate tier-1 supplier lines.
Pharmaceutical-grade belt conveyors must meet GMP, ISO 7 cleanroom, and ATEX zone requirements, with typical loads of 50-100 kg and speeds of 0.13-2.6 m/s for distribution duty. Selection hinges on belt material, cleanability, load class, and explosion-proof certification rather than throughput alon

Food-grade belt conveyors are specified by belt material, wash-down rating, throughput, and container geometry, with modular plastic, stainless metal, and fabric belts each owning a distinct duty band.

Belt conveyor selection for e-commerce fulfillment centers hinges on matching belt type, drive, and width to carton mix, throughput, and floor geometry. Light-duty plied PVC, modular plastic, and roller-gravity sections each fit a different node of the sorter-induction loop.
Dust collector systems split into dry (cyclone, baghouse, cartridge) and wet (scrubber) families, with sub-types selected by dust load, particle size, combustibility, and temperature. Baghouses dominate high-volume dry duty; cyclones pre-se粗; wet scrubbers handle combustible, sticky or soluble dust.

Choose a dust collector by matching airflow CFM, air velocity FPM, filter type, and dust combustibility to the application. Baghouse, cartridge, cyclone, and wet scrubber each fit a specific duty range; the wrong pick causes filter blinding, fire risk, or NFPA compliance failure.

UK manufacturers offer 150+ cardboard tube diameters with 3-day average delivery and BSI-approved QA, while Chinese suppliers on Made-in-China and Alibaba list MOQs from 100 to 1,000 pieces at US$0.12–$10.00 per unit across postal, industrial, concrete-form and cosmetic-pack grades.

Cardboard tubes divide into six functional families — postal, display, industrial core, mortar, concrete formwork, and bespoke printed — with over 150 standard UK diameters available and average 3-day delivery windows from in-house stock. Selection pivots on outer diameter, internal bore, wall thick

Cardboard tube selection turns on four numbers: inside diameter (8–500 mm), wall thickness (1–18 mm), length (5–8000 mm), and end-cap duty, matched to postal, core, or display use. UK manufacturer BMC confirms a 100-year-old product class still ships 100% recycled, FSC-certified material with no MOQ

Carrying cases divide into soft, hard, ATA-rated transit, and custom-foam equipment types, with HDPE, ABS, polypropylene, aluminum, ballistic nylon, and rotomolded polyethylene as the dominant shell and chassis materials. Selection hinges on payload value, impact rating, temperature exposure, and wh
Carrying case selection hinges on matching shell construction (EVA, vacuum-formed, blow-molded, plastic-injected, soft sewn) to payload weight, drop rating, IP target, and tooling budget. The five construction families documented in current OEM catalogs cover 90%+ of industrial carrying-case duty cy

Plastic containers are moulded packaging vessels made from polymer resins — primarily PE, PP, PET, PVC, PS and K-RESIN — and span 30 mL to 30 L capacities across food, medical, ESD and bulk-handling duties. Type selection is driven by chemical compatibility, temperature ceiling, transparency and dut
Pick plastic containers by matching polymer grade to duty: PP for microwave/freezer food, HDPE for chemicals, PET for clear beverage, LDPE for squeeze. Verify food-contact compliance, capacity in litres, and temperature limits before procurement.
China-based baler OEMs list 1,000-100,000 USD FOB price bands across 6 main types in 2026 listings. CE, ISO 9001, and Diamond/Audited tiers dominate the supplier pool on Made-in-China.com.

Selecting a baler machine comes down to matching drive type, chamber size, bale weight, and throughput to your scrap stream; horizontal hydraulic balers dominate metal recycling, while vertical or two-ram units fit lower-volume waste paper and plastic duties.

Global palletizer sourcing now spans European specialists and Chinese OEM clusters, with articulated robot palletizers dominating beverage lines at 6,000-10,800 bph and 155+ Chinese makers offering palletizers from US$12,586 to US$30,000 per set on Alibaba and Made-in-China.com.

Palletizer machine types split into robotic, gantry, and column configurations handling cartons, bags, bottles, and cases at 500-1800 cycles/hr. Selection hinges on payload, footprint, and end-of-line integration scope, not brand.

Choosing a palletizer in 2026 hinges on matching four-axis articulated robots, single-column, gantry, and high-level units to payload, SKU mix, and throughput. New Chinese-built robotic palletizers land between US$12,586 and US$35,000 per set, with MOQ of one unit.

Strapping machines split into semi-automatic, automatic, and pallet/press-arch categories, with PET/polyester strap dominating heavy-duty pallet lines at 9-12.5 mm width and 2,500 kg clamp tension. Selection hinges on throughput, strap material, and load compression, not marketing claims.
Chamber, thermoform-rollstock, tray-seal/skin-pack, and nozzle/belt vacuum packaging machines split the market by throughput and product geometry. Busch pumps, AISI 304 contact parts, UL/NSF certifications, and 10 m³/h tabletop class are the recurring spec bands across 2026 OEM listings.

Carton sealing machines and vacuum packaging machines serve different packaging stages: carton sealers close corrugated shippers at 15-30 cartons/min while vacuum sealers evacuate and heat-seal flexible pouches at 1-6 cycles/min for shelf-life extension. Cross-references the related /news/carton-sea

Carton sealing machine sourcing is dominated by Chinese OEMs offering taping units from US$9,800 and servo-adaptive folders near US$11,000, with FJ-1A-class sealers running at 20 m/min on 48-72 mm BOPP tape. Buyers should match drive layout, carton size envelope, and voltage to line duty before comp

Carton sealing machines split into manual, semi-automatic, and automatic categories sized by drive type, belt geometry, and case throughput. Spec-first selection maps FXJ/FXC 50-series semi-auto units at 15-25 cases/min against fully automatic case erectors and sealers in 30-80 cases/min ranges.
Carton sealing machine selection hinges on drive layout (left-right vs up-down belts), carton size range, and required throughput: semi-auto FXJ-5050 suits mixed-SKU lines under 20 cpm, while auto FXJ-AT5050 with pneumatic top-folding targets 30+ cpm continuous duty.
Stretch wrapping machine suppliers in July 2026 span roughly 130+ brands across DirectIndustry and 1,800+ Alibaba listings, with Chinese OEMs holding the largest SKU count and price-band breadth from US$500 to US$11,000+ per line.

Stretch wrapping machines split into six structural types — turntable, rotary arm, rotary ring, orbital, horizontal, and vertical — selected by load geometry, weight, and throughput. Current 2026 OEM data (768 catalog models across 135 suppliers) maps each architecture to specific pallet, profile, a

Stretch wrapping machines split into turntable, rotary arm, orbital, and robotic variants with pre-stretch ratios of 150-300%, throughputs from 20 to 200+ loads/hour, and pallet envelopes from 600x400 mm up to 2,600x3,600 mm. Pick by load weight, stability, throughput target, and film-yield economic

Shrink wrapping machines use heat-shrunk PE/POF film around products at 5-300 packs/min, while vacuum packaging machines evacuate air and heat-seal pouches for shelf life. Choose shrink for bundling/display, vacuum for perishable food, electronics, and oxygen-sensitive goods.
Automatic shrink wrapping machines with sealing bars run up to 600 p/h on film packs and 100 p/min on bottle/case collations, while semi-automatic bell-type units stay below 5 p/min for small-batch sealing applications.

Hydrostatic level transmitters (submersible HART/4-20 mA, 0-300 m range, ATEX/IECEx options) and dock levelers (mechanical/ hydraulic loading bays) solve unrelated problems — pick the former for liquid level in tanks/wells, the latter for truck-to-floor height compensation.
Capacitance level sensors (0-10 m range, 0-85°C, 316SS/Teflon probes, IS design) and dock levelers serve completely separate functions: liquid/slurry measurement vs. truck-to-warehouse bridging. Choose by application, not by brand.
An ultrasonic level sensor measures tank fill height via airborne ultrasound (0.07 m to 40 m range, IP67/IP68, ATEX options); a dock leveler is a mechanical loading-bay platform with hydraulic actuation. Use the sensor for liquid or bulk-solid level; use the leveler for truck-to-floor b

A guided wave radar (GWR) level sensor such as the BinMaster GWR-3000 is a TDR-based continuous level instrument rated 1–40 bar, –60 °C to +200 °C, IP68, with up to 22.86 m probe length, built for storage tanks and hazardous-area liquid interface measurement. A dock leveler is a mechanical loading-d

Four-axis palletizing robots handle 120-450 kg payloads at ±0.2-0.5 mm repeatability with IP65 protection, while AGV robots move finished pallets autonomously along fixed or SLAM-guided paths, making them complementary rather than competing assets in end-of-line material flow.

Collaborative robots (cobots) are fixed-base, force-limited manipulator arms designed to share a workspace with humans, while AGVs/AMRs are mobile platforms that transport payloads between stations. They solve different problems and only overlap in mobile manipulation cells where both are combined.

Delta robots are fixed-base parallel pick-and-place arms reaching 150 CPM at ±0.2 mm repeatability; AGV robots are mobile carriers that move whole payloads across a facility. Use delta for high-speed stationary picking, AGV for inter-station transport. They complement, not replace, each other.

SCARA robots handle fixed-station pick-and-place with 5-20 kg payload and 650 mm reach, while AGVs move materials across the factory floor. They are complementary, not competing, classes — choosing depends on stationary precision versus mobile transport needs.
Articulated robot arms (6-axis, 0.5-40 kg payload, 0.01-0.05 mm repeatability) suit fixed work cells, while AGVs move material across floors via guided paths. Pick an arm for precision manipulation; pick an AGV for payload transit between cells.

Crawler cranes lift 3,000+ tons on tracked undercarriages at 1-2 km/h, while stacker cranes shift 1-5 ton loads inside automated warehouses on rails up to 40 m. Pick the first for outdoor heavy lifts, the second for indoor pallet flow.

Mobile cranes and stacker cranes occupy distinct lift-handling niches: mobile cranes serve outdoor, mobile, variable-radius lifting under BS EN 13000, while stacker cranes are fixed-aisle automated storage/retrieval units. Choice hinges on duty cycle, footprint, lift envelope, and whether loads are

Tower cranes lift 4-600 t loads outdoors on construction sites at 35-150 m hook heights; ASRS stacker cranes move 0.5-5 t pallets inside high-bay warehouses on fixed rails. Pick by load class, lift envelope, and whether the work happens outside on a job site or inside a rack aisle.
Gantry cranes serve outdoor heavy-load lifting on ground rails with spans of 5–35 m and capacities to 80 t, while stacker cranes run inside automated warehouses on fixed aisle rails with vertical mast lift heights often exceeding 40 m. Choose a gantry crane for open yards, shipyards, and container h
Overhead bridge cranes span 5-60m and lift 1-500t across fixed factory aisles; stacker cranes store pallets in narrow aisles to 40m+ heights. Choose overhead bridge for heavy tonnage and open spans; pick stacker for high-density warehouse storage. The two serve different load and footprint profiles.

Screw conveyors handle enclosed, short-distance bulk transfer of dusty, hot, or odorous material with multiple discharge points; belt conveyors move higher volumes over longer distances and inclines with lower power draw per ton. Selection hinges on material properties, distance, angle, and dust con

Chain conveyors and belt conveyors both move unit loads, but chain conveyors handle heavy, hot, or oily parts with metal slats/top chains while belt conveyors (PVC/PU/rubber) win on hygiene, noise, and energy per meter. Match the conveyor to load geometry, temperature, sanitation class, and layout b
Roller conveyors handle unit loads via gravity or motorized rollers (Ø30-60 mm, 100-2,500 mm length, 72-1,500 N load), while belt conveyors use a continuous belt for bulk and irregular items over longer runs. Pick roller for cartons totes and zero-pressure accumulation zones; pick belt for aggregate

A five-year TCO model for a wire-mesh storage cage is dominated by three drivers — steel substrate and finish, deployment volume, and fork-truck damage rate — with purchase price typically representing only 40-55% of lifecycle cost on industrial sites.

Stackable storage cages cut warehouse footprint 60-75% versus loose pallets and pay back in 6-18 months, but 2-3 year service life and forklift damage make them uneconomic for hazardous, high-turnover, or 5+ year fixed installations.
Foldable wire-mesh storage cages stack 4-high at roughly 1,000 kg per tier when specified correctly, but installation success hinges on floor flatness, M12 anchor torque, and 1.5× load testing before commissioning. Skip those gates and rack collapse risk jumps sharply on uneven concrete.

Storage cages fall into five practical families—stacking, foldable, caster, tow, and heavy-duty—distinguished by wire diameter (typically 4.8–6.4 mm), mesh opening (25×25 to 100×100 mm), and base construction (U-channel or angle/rectangular tube). Selection hinges on load, mobility, and reconfigurat
IBC tanks (intermediate bulk containers) deliver the lowest cost-per-litre of any reusable liquid packaging in the 600-1,500 L range, but only when their UN rating, stack load, and chemical compatibility match the service — otherwise leakage, blow-mould stress cracks, and pallet-bottle mismatch beco

A 1000 L UN-certified IBC tote installs in three controlled stages — siting and base prep, frame leveling, and fill/vent line hookup — with HDPE inner container, galvanized or stainless steel cage, and pallet specified for Class II or lower dangerous goods at 1.6 SG nominal filling density per Hawma

Standard IBC tanks ship in 275-gal and 330-gal volumes on a 45"x45" pallet footprint, classified by material (HDPE composite, carbon steel, stainless steel) and UN/DOT 31A certification for Packing Group II/III liquids. Selection hinges on chemical compatibility, specific gravity (≤1.5 stackable, ≤1

FIBC bulk bags deliver 5:1 to 6:1 collapse-to-product volume savings and reusable transit economics, but trade off against moisture sensitivity, single-trip fatigue, and forklift handling constraints. Spec gate: UN-certified bags for hazardous goods, food-grade liners for ingestibles, 5:1 SF for sin

FIBC bulk bag installation hinges on five design decisions — body type, lift loop style, fill/discharge spout, safety factor (5:1 or 6:1), and UN/ESD certification — matched to load, density, and atmosphere.
FIBC bulk bags are classed by electrostatic safety (Type A/B/C/D), UN packaging groups for hazardous goods, body construction (U-Panel, Circular, Baffle, 4-Panel), and top/bottom fill-discharge geometry (duffle, spout, open). Selecting the right type is a hazard-class-and-product-fit decision, not a

A real carton box TCO is 3-6x the unit purchase price once freight, palletisation, return logistics, and damage write-off are added over a 12-36 month window. Corrugated single-wall, double-wall, and heavy-duty triple-wall options split sharply on cost-per-trip, not on per-box sticker price.
Carton boxes are classified by flute profile (single/double/triple-wall), board grade (ECT vs Mullen), style (RSC, HSC, FOL, telescope, partition), and load rating. Spec-driven buyers match flute + ECT to Gross Weight to Edge Crush Test per TAPPI T 811 and Box Maker's Certificate (BMC) markings.

Strapping band total cost of ownership is dominated by band material (PP vs PET vs steel), strap width and thickness, joint type, and consumable replacement cycles. A TCO model covers acquisition, tooling, labour, downtime, and waste over a 3-5 year window, not just roll price.

Strapping band — steel, PET, PP and woven types — delivers high tensile strength and low unit cost for pallet and bundle unitisation, with trade-offs in tooling cost, recoil hazard, and end-of-end recyclability. The right spec depends on load profile, tension method, and downstream recycling gate.

Strapping band classification splits into three commercial families: polypropylene (PP), polyester (PET), and steel, each mapped to a load range, elongation behaviour, and joining method. PP sits at the light-duty end, PET handles the medium-to-heavy pallet tier, and steel still owns the highest bre

Stretch film TCO over a 3-5 year window is dominated by 4-6 cost drivers: film cost (60-75%), pre-stretch equipment depreciation (10-15%), labor (8-12%), film waste, energy, and pallet damage claims. Hand wrap vs. machine wrap differs 3-5x in film cost per pallet.
Stretch film installation hinges on matching LLDPE gauge and width to load weight, then applying 250-300% stretch with proper overlap. Cast film suits quiet, high-clarity hand wrap; blown film wins for sharp-edged, heavy pallet loads. Pre-stretch at 80% for uniform light cartons.
Stretch film divides into hand (manual), machine, pre-stretch, and PCR-recycled grades, with sub-types including stiff, extended-core, jumbo, mini, black, and food-contact variants; selection hinges on gauge, load profile, and wrap method per manufacturer data published 2025-2026.

A turnover box's true 5-year cost is dominated by cleaning labour, write-offs, and freight weight, not the unit price. PP corrugated and foldable insulated variants typically beat one-piece HDPE in TCO over 200+ cycles.

Turnover box installation in 2026 hinges on matching the container family — corrugated PP, HDPE, EU-stacker, or insulated cold-chain — to racking pitch, dynamic load, and ingress rating, then torquing label clips to 2.5–4 N·m on PP drop-doors. Common failure modes are hinge cracking above 80 kg dyna
Plastic turnover boxes fall into five structural families — solid-wall, foldable/collapsible, ventilated, stack-nest, and pallet-box — built mainly from PP or PE injection-moulded parts, with selection driven by load class, temperature window, and return-loop logistics rather than by single-buyer ec

Plastic pallets, typically HDPE or PP, last 5-10x longer than wood, weigh 15-30 lbs, and resist moisture/chemicals, but cost 2-3x more upfront, deform under heavy static loads, and shed microplastic fibers. HDPE wins chemical/impact duty; PP handles higher heat; PLA biodegrades but fails above 55-60

Plastic pallet installation follows four gates — floor flatness, racking compatibility, load class, and forklift interface — with HDPE/PP nestable, rackable and stackable variants defined by dynamic load ratings from ~1,000 kg to over 5,000 kg per ISO 8611.

Plastic pallets split into structural families — nestable, rackable, stackable, and export/one-way — with load ratings from 700 kg racking to 3,000 kg static, in 1,200x1,000 mm Euro, 1,140x1,140 mm ISO, and custom footprints.
Bench scale installation hinges on five physical decisions: platform size, capacity, frame material (mild steel vs 304 SS), load-cell rating with 150% safe overload, and indicator pairing. Get those right and a TN-class platform at 30×30cm to 60kg or 46×46cm to 600kg drops onto a workbench in under

Bench scales are classified by capacity, resolution, indicator type, and IP rating into counting, checkweighing, compact, and platform-integrated models, typically spanning 0.6 kg to 600 kg. Selection hinges on environment, readability, throughput, and connectivity rather than capacity alone.
A filling scale's true lifecycle cost runs 3-5x the purchase price once calibration, CIP, energy, spares, and downtime are amortised over a 10-15 year service life. The biggest TCO drivers are weighing accuracy drift, washdown rating, and PLC integration, not the head unit itself.
Filling scales deliver 0.1-0.5% repeatability on bag, jar, and bottle lines but cap at 5-10 packs/min, making them a fit for low-to-medium runs and a poor choice for high-speed beverage or pharmaceutical lines above 60 packs/min.

Filling scales split into five operating classes by automation level — manual, semi-automatic, fully automatic, multi-head combination, and inline checkweigher-integrated — with selection driven by throughput, container format, accuracy class, and OIML R76 / R61 compliance rather than a single best

Checkweighers deliver ±0.1–0.5 g precision at 60–600 ppm throughput and cut giveaway cost by 1–5% of product weight, but they add 0.3–1.5 m of conveyor length, 1.5–6 kW power draw, and require regular load-cell calibration to stay in statistical process control.
Electronic truck scales (weighbridges) deliver 10-200 t weighing capacity at OIML III accuracy, but require permanent concrete foundations and add 150% safe-overload headroom only. Pit-mount, surface-mount and axle scales each trade civil-works cost, throughput, and axle-compliance risk differently

A 2026 carton erecting machine TCO review must price the PLC-controlled unit, the servo drives, the tooling, compressed air, and the labor for changeovers. This breakdown ranks the seven cost drivers, lines up single-station vs double-station models, and quantifies the 5- to 10-year spend envelope.

A carton erecting machine installs in 4-8 hours on a flat 15-20 MPa floor with 6 bar clean dry air, 380 V 3-phase 50 Hz power, and 3000 mm clearance for blank stack feed. Acceptance target is ±0.5 mm flap-fold accuracy, ≥15 cycles/min, and CE-conformant guarding per EN 415-8 safety of packaging mach
Carton erecting machines split into three structural classes — single-station, double-station, and inline thermoforming — differentiated by servo vs mechanical drive, output from 30 to 180 pieces/min, and CE compliance for EU-bound food packaging lines. Spec-driven buyers should match station count,
A vacuum packaging machine's TCO over a 5-7 year window is dominated by 5 cost drivers: pump type (oil-sealed vs dry rotary vane vs bushed), chamber-vs-belt throughput, seal-bar maintenance, electricity per cycle, and bag/film yield. Busch's TCO framework flags energy, spares, downtime, and disposal
Chamber vacuum sealers extend shelf life and reduce product damage, but trade off bag cost, throughput ceilings, and shape limits against modified-atmosphere or heat-seal alternatives. Floor-type models cycle 40-60 s at 20 m³/h pump capacity on 220 V single-phase supply.

Vacuum packaging machine installation follows a six-step field sequence: site and power prep, vacuum pump commissioning, seal-bar calibration, gas-flush check, and acceptance test. Thermoforming units draw 10-20 kW at AC380V/50Hz/3P and require a BUSCH rotary vane pump primed to 1/2-3/4 oil window.
Shrink wrapping machine TCO is dominated by four cost drivers: film and energy over 7-10 year life, plus initial capex tied to throughput and a film-size envelope. The SITMA WM60 lists a 3,600 p/h mechanical ceiling and a 75-420 mm width range, illustrating how spec choices ripple into long-run cost

Shrink wrapping machine installation centres on site prep, power/air supply, film threading, and shrink-tunnel commissioning. Specs pulled from 2026 OEM catalogues show throughput from 0–80 p/min, widths 350–1,480 mm, and air demand up to 8 CFM @ 75 PSI on semi-auto units.

A case packing machine automates secondary packaging by collating, loading, and sealing products into corrugated or paperboard cases, replacing manual case loading at throughputs typically between 10 and 200 cases per minute depending on configuration. The trade-off is clear: capital and footprint c

Case packing machine installation runs through a fixed five-stage sequence: site prep, infeed alignment, mechanical mounting, commissioning, and acceptance testing. Standard electrical, pneumatic, and floor-load requirements must be met to prevent downtime and ensure CE, EMC, and LVD compliance.
Case packing machines are classified into top-load, side-load, wrap-around, robotic, horizontal and vertical formats, with throughputs spanning roughly 10–300 cases/min depending on automation level. Selection hinges on product geometry, line speed, case style, and integration with upstream filling
A correctly specified and mechanically aligned labeling machine line reaches ±0.5 mm label-placement accuracy at 30-200 BPM; most installation failures trace to foundation, leveling, conveyor squareness, and PLC/HMI signal noise, not the labeler itself.
Labeling machines split into four structural families — manual/semi-automatic, inline (linear), rotary, and specialty (roll-fed, cut-and-stack, RFID/EAS) — chosen by container geometry, throughput, and label format. Spec sheets published through 2026-07 place inline and rotary systems above ~10,000

Capping and sealing machine TCO is driven by five lifecycle cost buckets — purchase, changeover/setup, spares, energy, and unplanned downtime — and over a 10-year horizon downtime and spares typically outweigh the headline price. This article breaks down each driver with concrete figures and an opti

Capping and sealing machines deliver 6,000-30,000 bottles/hour throughput with torque accuracy to ±0.2 N·m on rotary cappers, but capex of US$35,000 and up per station, format-change downtime, and cap-geometry sensitivity make them uneconomic below mid-volume runs.
Induction cap sealers (Enercon Super Seal™ 300/400/600) anchor most non-aseptic lines; pressure-cap sealers (300 ml silica-gel class) handle viscous/inert-gas fills. Five-gate spec map, Foil/closure torque targets, and 1.5–2.0 mm air-gap window drive acceptance.

Filling machine TCO is driven by the purchase price, five operating-cost streams (energy, CIP, changeover, reject, downtime), and end-of-life disposal, not by the headline quote. A credible lifecycle model should be re-baselined annually, not run once at award.
A correct filling-machine install follows five gates: site prep with 380 V three-phase + 0.5-0.7 MPa clean air, leveling to 0.1 mm/m, CIP/SIP loop pressure-test to 0.6 MPa for 30 min, a 2-hour no-load commissioning run, then weight-based ±0.5 % accuracy validation. Skip any gate and you accept chron

Coding machine TCO spans five cost drivers: acquisition, consumables (ink/ribbon/solvent), maintenance labor, throughput-driven energy, and end-of-line changeover loss. Lifecycle math over 5-10 years typically puts consumables and labor at 55-70% of total cost, dwarfing the 15-25% sticker share.
Industrial coding machines split into three mechanical families — contact, non-contact inkjet, and laser — classified by integration mode (offline vs. inline) and by print-technology class. Selection hinges on substrate, line speed, mark permanence, and print resolution rather than brand.

Strapping machine total cost of ownership is dominated by lifecycle costs, not purchase price: strap material, energy, maintenance and downtime typically outweigh the machine over a 10-year horizon. Sourcing rules: match arch (PP vs PET), tension class and duty cycle to product class; verify seal me

Strapping machines automate tensioning, sealing, and cutting of PP, PET, or steel strapping band around cartons, pallets, and bales, with high-speed servo-driven units reaching 26 single-pass cycles per minute, cutting labour versus manual hand-tying. Trade-offs include capital cost, strap-material

A correct strapping machine install rests on five checkpoints: foundation/level, power/PE grounding, air supply, strap path calibration, and safety-circuit verification. Skipping any one of the five is the most common root cause of cycle-fault downtime on PP-strap pallet lines.

Strapping machines are classified by automation level (semi-automatic vs. fully automatic), arch geometry, and seal method (heat-weld vs. metal buckle), with PP and PET band widths typically 9-19 mm.

A wrapping machine's true 5- to 10-year cost is 2–4× its purchase price once film, energy, spares, and downtime are tallied. Engineers who skip a TCO model typically under-budget consumables and over-budget the capex line. Build the model around four cost drivers: film-grade chemistry, thro
Wrapping machines cut secondary-packaging labour by automating film application across pallet, carton, reel, and tire formats, with trade-offs in film yield, footprint, and capex. Selection pivots on load geometry, throughput, and whether the line needs stretch, shrink, or orbital wrap.
Order pickers lift operators and pallets to elevated pick positions in narrow-aisle warehouses, cutting travel time and increasing picks per hour, with electric models typically reaching 6-12 m lift heights and manual variants 1.5-2.5 m. The trade-off is higher unit cost, stricter floor-flatness req

Order pickers span four core classes — counterbalance, reach, turret/VNA, and order-picking high-level — classified by mast travel, aisle width, and lift height. Selection hinges on rack depth, pick face height, and throughput, with electric AC drives now standard for indoor warehouse duty. Safety i

Reach trucks deliver 8-12 m lift in 1.2-1.5 m aisles and cycle 30-50% faster than counterbalance forklifts, but their cost, single-direction travel, and dependence on flat smooth floors make them a poor fit for outdoor or mixed-load sites.

Dock leveler total cost of ownership spans purchase, install, energy, maintenance, downtime, and disposal across a 15-25 year service life. The acquisition price typically represents 25-40% of lifetime cost, with hydraulics, controls, and duty cycle driving the remainder.

Hydraulic and mechanical dock levelers each trade specific strengths against specific weaknesses. Hydraulic units deliver faster cycles and higher capacity up to 60 kN load class, while mechanical units cut acquisition cost and eliminate hydraulic-fluid contamination risk.

Hydraulic, mechanical, and air-powered dock levelers each demand a distinct pit-spec, anchor-bolt, and lip-extension sequence; capacity ratings from 2 to 12 tons and ANSI MH30.1 performance testing govern U.S. heavy-load installs.

Dock levelers fall into three primary actuation classes — hydraulic, mechanical (spring/counterbalance), and air-powered — with vertical-storing and edge-of-dock variants layered on top. Selection hinges on duty cycle, capacity, pit depth, and the height differential between warehouse floor and truc

A platform trolley is a manual or powered wheeled cart designed to move palletised, boxed, or bulk loads across a facility floor. Its core advantages are low unit cost, no licence requirement for manual versions, and high manoeuvrability; the dominant disadvantages are manual operator fatigue, load-

A correctly installed platform trolley depends on a flat, level floor, four-point load-matched caster selection, locked swivel casters at the rear, and a working load limit verified at 1.5x the rated capacity before service.

Industrial platform trolleys split into four main duty classes — light-duty (≤150 kg), medium-duty (300–500 kg), heavy-duty (1000–2000 kg), and tow-line / track-guided systems — driven by deck size, wheel diameter, and frame material. Selection hinges on load, environment, and handling model rather
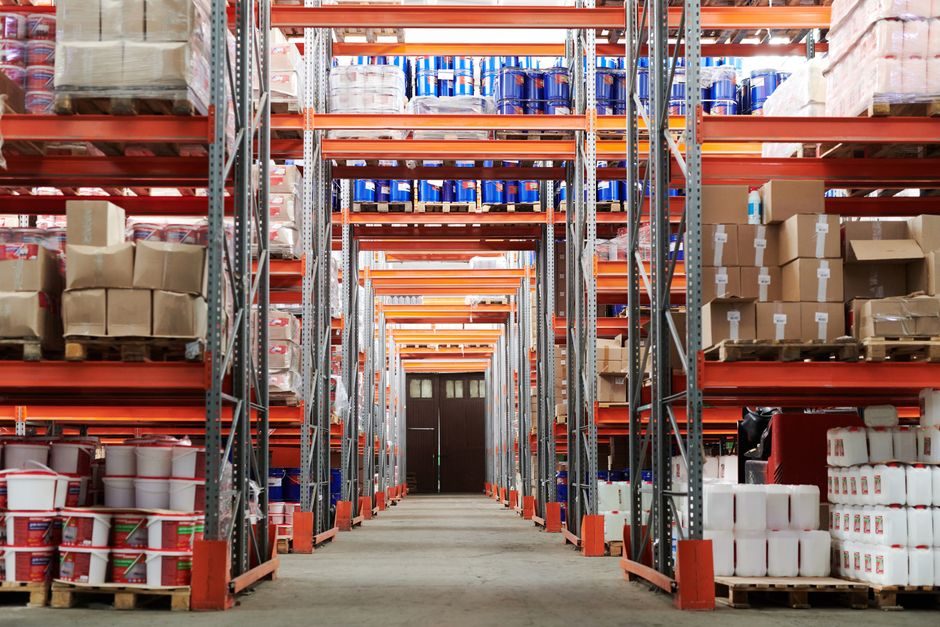
Manual pallet jacks lift 2,200–5,500 lb at the lowest cost-per-unit of any warehouse lift tool, but operator strain, slow throughput above ~50 pallet moves/shift, and floor damage make them a fit only for low-frequency, short-haul duties. Choose manual for under 150 pallets/day on flat concrete; swi
Manual pallet jacks (capacity 2.5–3.0 t, fork length 550–1220 mm) install in 10–15 minutes: uncrate, bleed the hydraulic cylinder, adjust the 3-position control lever, and verify the entry/run-in height against the 85 mm Euro pallet spec. Site prep covers floor flatness (≤3 mm/m), load-wheel wear (≤

Manual pallet jacks are classified by fork length, load rating, wheel material, and pump mechanism, with standard hand pallet trucks rated 2,200-2,500 lb, heavy-duty units reaching 3,500 kg, and specialized stainless/corrosion-resistant models for chemical and food plants. Choose by fork span, capac
Pallet stacker TCO over a 7-10 year service life is dominated by energy, batteries, planned maintenance and operator labour rather than purchase price; a Crown DT-series 2 x 1000 kg double stacker typifies the class with travel speeds up to 12.5 km/h and rider/pedestrian convertible control.
Pedestrian, stand-on, ride-on, seated, and automated pallet stackers split into five clear duty classes, with electric 24 V Li-ION models dominating 1.0–2.0 t walkies and 1.4–2.0 t riders per 2026 OEM line-ups. Selection pivots on load, lift height, aisle width, and operator ergonomics, not horsepow

Electric pallet trucks cut manual handling effort and lift 2,000–12,000 kg loads on 24 V platforms, but they add battery, charger and controller cost versus a hand pallet jack. The right call is workload volume, aisle width and grade, not a blanket yes.

Electric pallet truck installation hinges on rated load (typically 2,000-3,000 kg at 600 mm load center), fork dimensions, battery voltage (24V/48V), turning radius, and floor gradient limits. Site prep requires flat concrete ≥C25/30, 1.5x truck-length approach clearance, and a 10-15 A dedicated 110

Electric pallet trucks split into five operator-position classes: walk-behind, fold-down platform, fixed platform, stand-on, and radio-controlled, with 24 V systems dominating the 1.3-2.5 t segment and 80-465 Ah batteries setting the autonomy envelope.
AS/RS systems split into four structural classes — unit-load, mini-load, vertical lift module (VLM), and carousel — selected by SKU profile, footprint, and throughput. Each class carries distinct height, payload, and SKU-density envelopes that drive specifying-engineer decisions in 2026.

A conveyor sorting line TCO analysis spans 10-15 years and bundles capex (30-40% of spend), energy (15-25%), spares and maintenance (20-30%), and labor. Hidden cost drivers—divert wear, belt tracking, control retrofits—often double the integrator's original quote.

Conveyor sorting line installation follows a four-step site acceptance path — line check, pressure test, flush, and re-installation inspection — anchored to P&ID tag lists and MCCR punch lists, with pre-engineered components and 24-hour spare-part shipping available from full-line integrators.

Conveyor sorting lines split into two top-level families — line sorters and loop sorters — differentiated by induction count, recirculation, and divert mechanism. Selection hinges on item size, divert rate, and accuracy rather than brand.
Sorting-system TCO over a 10-year horizon is typically dominated by 70-80% lifetime operating cost versus 20-30% acquisition; the largest cost drivers are throughput, sortation accuracy, downtime, energy, and lifecycle maintenance.
Industrial sorting systems pair high-throughput conveyors, optical sensors, and PLC logic to deliver measurable throughput gains, but introduce capex, sensor limitations, and integration risk. Selection hinges on SKU mix, accuracy target, and required sort categories per minute.
Vertical lift modules (VLMs) reclaim up to 85% of floor space by storing totes in vertical columns with a single extractor, but carry high capital cost, ceiling-height dependence, and a single-point-of-failure lift that buyers must weigh against faster picking and 24/7 inventory accuracy.

Vertical Lift Modules (VLMs) are enclosed automated storage systems that deliver trays to an operator bay, classified by unit height, tray payload, and delivery configuration. The market spans compact slim models under 16,100 mm unit height up to 990 kg per-tray payload, with single- vs dual-deliver
A shuttle system TCO model spans a 10–15 year life cycle where hardware, controls, energy, and unplanned downtime split roughly 15:25:20:40 of total spend. The purchase line is the smallest bucket; energy and the maintenance labor tied to battery, drive and rail wear are the largest levers.
Shuttle systems—rail- or track-guided carriers moving pallets between rack aisles—deliver high-density storage at throughputs between 60 and 300 pallets/hr per aisle, but cap vertical access at one level per carrier and require aisle infeed discipline. They outperform unit-load ASRS on cost-per-pall

Pallet shuttle system installation is a structured, contractor-led project spanning site survey, rail-aligned rack build, shuttle commissioning, and 1–2 weeks of on-site operator training. Skipping laser rail alignment, slab checks, or pallet-quality gating causes jams, sensor faults, and spec-sheet

Autonomous Mobile Robot (AMR) total cost of ownership hinges on five cost lines — hardware, software/fleet, integration, energy and maintenance — and is typically dominated by a 7-10 year operational phase, not the unit price. Buyers should benchmark payload, fleet size and duty cycle first, then ru
AMRs replace human transport runs with sensor-guided, 24/7 mobile units but require a 6-18 month payback runway and a structured facility to deliver it. The right call: AMRs fit high-mix, high-volume intralogistics; they underperform on heavy outdoor hauling and tightly fixed routes.
Autonomous mobile robots (AMRs) are classified by navigation method, drive configuration, payload class, and operating environment, with intralogistics units typically handling 50–500 kg via ROS 2-based SLAM.

Selective pallet racking delivers the highest pick-face density per square metre of any forklift-served rack system, but it ties a warehouse's vertical clear height, forklift class and floor-flatness tolerance together — a fact buyers confirm before any quotation. This reference lays out the load, s

Pallet rack installation in a 400,000 sq ft distribution center typically runs 2-3 weeks with certified crews, requires RMI/AS4084/FEM-spec compliance, and must include base-plate anchoring, frame plumb checks, and load-disclosure signage before any pallet is loaded.
Pallet rack systems fall into six structural families — selective teardrop, drive-in, push-back, pallet flow, cantilever, and mobile — each defined by beam-to-upright geometry, load class and aisle logic, not by brand.

An AGV fleet TCO model is built from 8 cost lines — unit, integration, batteries, software, energy, service, downtime, and residual — and over a 10-year life the running-cost block (energy + service + downtime) typically dwarfs the unit price on most plants.
AGV robot installation is a site-engineering job, not a plug-and-play one: floor flatness, magnetic-tape or QR-code layout, battery room sizing, and PLC/WMS handshake define the 2-4 week commissioning window for a typical 500-2000 m² cell.

AGV robots split into five load/form-factor classes — unit-load, tow/tug, fork, heavy-duty and assembly — each mapped to a navigation stack (magnetic tape, QR/2D code, LiDAR SLAM, contour or natural feature), and selected against payload, aisle width, ISO 3691-4 safety class and floor-marking tolera
Stacker crane TCO over a 20-25 year service life is dominated by energy and maintenance (60-80% of lifecycle cost), with acquisition typically only 10-20%. Use an 8-line cost model with documented discount rate, downtime valuation, and kWh rate to compare SRM, ASRS and mini-load classes.

Stacker cranes deliver 30-50% higher storage density than counterbalanced forklifts in AS/RS builds, but cap at roughly 40 m lift and demand tight aisle tolerance of ±10 mm. Right call for high-throughput pallet warehouses; wrong for mixed-load yards and outdoor docks.

AS/RS stacker cranes are typically engineered into a 30 m+ high-bay envelope and qualified to ISO 9001/ISO 14001 management regimes, with the structural and electrical checks anchored in TSG Q7016-2008. Pallet, miniload and long-load variants diverge on load (0.15 t to 40 t), aisle geometry and WMS/

Stacker cranes split into three structural families governed by ASME B30.18-2016: top-running and under-running bridge configurations, with mini-load, unit-load and heavy-load subclasses for boxes, pallets and ton-scale goods.

Vibrating conveyors move bulk material on a driven, slightly inclined trough using controlled mechanical oscillation, and the same oscillation that handles hot, abrasive or fragile loads is the source of their characteristic drawbacks: structural vibration, noise, and limited conveying distance.
Vibrating conveyors move bulk solids on a driven, oscillating trough with no internal moving parts, suiting abrasive, hot or sanitary duties; trade-offs are higher drive power per ton, vibration transfer to structures, and limited performance on wet, sticky or fragile feeds. Spec the unit by trough
Install a vibrating conveyor as a directional-jump linear system: twin matched vibration exciters, an isolation-spring set, and a trough mounted on a steel or fabricated base. Match trough geometry to the bulk material, then verify stroke, frequency, and amplitude under load before commissioning.

Vibrating conveyors are classified by trough geometry (horizontal, inclined, tubular), drive type (vibrator motor vs. exciter), and isolation method, with three primary form-factors dominating industrial spec sheets.

Pneumatic conveying TCO is dominated by 10-20 year energy and compressed-air costs, not the blower purchase price. Spec dense-phase over dilute-phase above 50 t/h to cut specific energy use.
Pneumatic conveying moves dry bulk through pipelines using airflow, with dilute phase typically running below 1 bar pressure drop and dense phase capable of longer distances at higher line pressure. Energy use, material degradation, and velocity limits define where the technology is the right fit.
Field installation of a pneumatic conveying system turns on five gates: phase selection, material characterisation, line geometry, dust collection and commissioning. Skip any of them and the system either plugs, erodes the bend wall, or fails ATEX area classification on handover.
Bucket elevators move bulk solids vertically with low footprint and high capacity, but trade off against dust, wear, and high head-shaft power. Spec gates: capacity 5–600 m³/h, lift 10–60 m, belt speeds 0.5–2.5 m/s, CEMA No. 300–700 buckets.

Bucket elevators split into centrifugal-discharge, continuous, and positive-discharge designs, with belt vs chain, steel vs polymer bucket, and J/D/AA/CC-S pattern codes driving real selection decisions on lift height up to 50 m and bulk density.

Overhead conveyor TCO is dominated by energy, chain/trolley wear and maintenance labor, not purchase price — typical 10-year run-rates show energy and service at 55-70% of lifecycle cost when amortised correctly. Spec the drive, chain pitch and trolley lubrication interval first; everything else is

Overhead conveyors use ceiling-suspended tracks to move loads through paint, finishing and assembly lines, freeing floor space but introducing structural load, obstruction and maintenance trade-offs that buyers must verify against load, layout and code.
A mesh belt conveyor is installed by verifying a flat straight guide rail first, then tensioning the belt, aligning sprockets, and running a no-load commissioning check. Common belt specs span -100 °C to 1,200 °C service, widths up to 6,000 mm, and pitches of 2.7-80.0 mm.

Mesh belt conveyors split into two main families — woven metal mesh for high-heat furnace and heat-treat lines, and PTFE-coated fiberglass mesh for drying/UV ovens — with weave pattern, edge type and drive method defining the sub-classes engineers specify.

Chain conveyors move heavy, abrasive, hot or oily unit loads on a positive-drive linked chain wrapped over sprockets, delivering high load capacity, steep incline capability and oil/dust tolerance at the cost of noise, wear and higher drive power. Decision rule: specify chain conveyors for harsh-dut

Screw conveyor total cost of ownership is driven roughly 70-80% by energy, wear-part replacement and downtime, not the purchase price, with motor kW, bulk density, abrasion index and hanger-bearing spacing the dominant design levers.

Roller conveyor TCO over a 10-year horizon is dominated by energy and maintenance, not acquisition; typical installed-frame purchase covers only 15-30% of lifecycle cost, with bearings, motors and bearings-lubrication cycles driving the balance.

Belt conveyor TCO analysis quantifies acquisition, energy, spares and downtime spend across a 20–30 year service life, with idlers, belt cleaners and vulcanised splicing commonly driving 60–80% of lifetime cost.
Belt conveyors move bulk or unit loads on a continuous belt looped over drive and idler pulleys, with typical belt-width ranges of 500-2400 mm and speeds of 0.5-6.5 m/s; their main advantages are high capacity and low energy per ton, while their disadvantages centre on belt wear, mistracking and dus
Belt conveyors are classified by form factor (flat, inclined, curved, Z-type, troughed) and load range, with ordinary units limited to slopes below 18° and large-inclination units reaching 38° design / 33° applied angle.

Gravity roller conveyors carry unit loads of 1–500 kg on spun-steel or polymer rollers at speeds up to ~1.5 m/s; they are the lowest-cost, gravity-fed handling option but fail with soft-bottomed, oily, or irregular loads.

55-gallon (208 L) drum sourcing in 2026 splits into three material tracks — steel (carbon/stainless), HDPE plastic, and laminated steel — with China-based manufacturers and Alibaba aggregating most global supply.
A standard 55-gallon drum measures 33–36.75 in tall and 22.375–24.5 in diameter, ships in steel, HDPE or fiber builds, and is paired with matched accessories such as 1600 W silicone heaters, 1200 lb dollies, and Brady SKA-55 spill kits.

Corrugated boxes are engineered fiberboard structures with flute profiles ranging from A-flute (~33 flutes/ft) to F-flute (~128 flutes/ft), built as single-face, single-wall, double-wall or triple-wall boards to match load weight, stacking and printing needs.
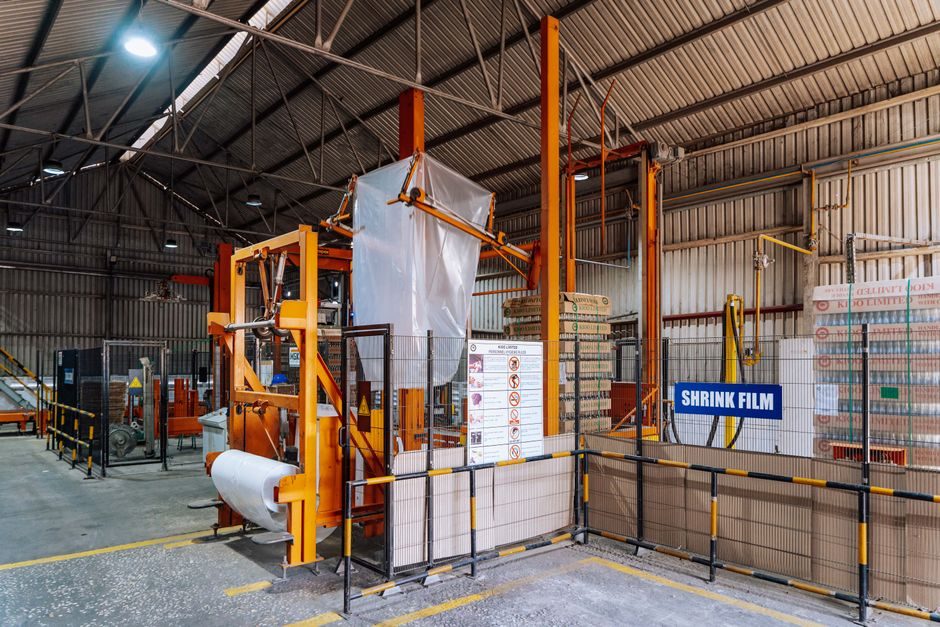
Industrial palletizer prices on the China B2B market range from roughly US$7,860 for entry-level collaborative units to about US$78,000 for high-speed automatic robotic arms, with most standard robot palletizers clustering between US$11,000 and US$40,000 per set as of 2026-02 to 2026-06.
Carrying case pricing in 2026 spans US$1.50 for 100-piece-MOQ EVA zipper pouches to US$380 for industrial aluminium flight cases, with material, MOQ and tooling driving the spread.

Strapping machine selection hinges on four decisions: manual vs automatic cycle, strap material (PP vs PET vs steel), throughput in packages-per-minute, and top-press for compression. Match machine class to load profile, verify strap width range and tension, then qualify the supplier on service.

Dust collector selection is governed by three quantifiable parameters: airflow (CFM) matched to tool port size, static pressure (typically 3" w.c. / 7.5 hPa filter-loaded threshold), and filter media class — baghouse, cartridge or cyclone — chosen for dust explosivity and loading rate.

Carrying case selection hinges on matching four engineering variables — payload mass, drop height rating, environmental seal, and material forming process — to your product's ISO 13485, REACH, or RoHS compliance path, with MOQ tiers from 1-piece retail to 500+ custom industrial runs.

Plastic container prices on Chinese B2B platforms in May-June 2026 range from US$0.03-0.05 per unit at 5,000-piece MOQ for small medical containers, US$6.50-7.00 per piece for acrylic display boxes, and US$900-1,030 per ton for raw resin — driven by MOQ, material and audit tier.

Plastic container selection hinges on resin family (HDPE/PP/PET), UN dangerous-goods rating, capacity class, and load geometry. As of 2026-07-12, 1000 L HDPE IBC tanks remain the industrial bulk standard at 1200x1000 mm footprint, while 54 L stackable bins and IML food containers dominate SME handli
Corrugated box selection hinges on flute profile, ECT rating, ply count and box style; matching those four to product weight, drop height and stack load avoids 80% of damage claims.

Turntable, rotary-arm, and orbital stretch wrappers split the industrial pallet-packaging market by load weight and throughput: turntables up to ~2400 mm table diameter suit loads under 2000 kg, rotary arms serve tall/light loads up to ~1600 mm wrap height, while 250% pre-stretch film carriages now
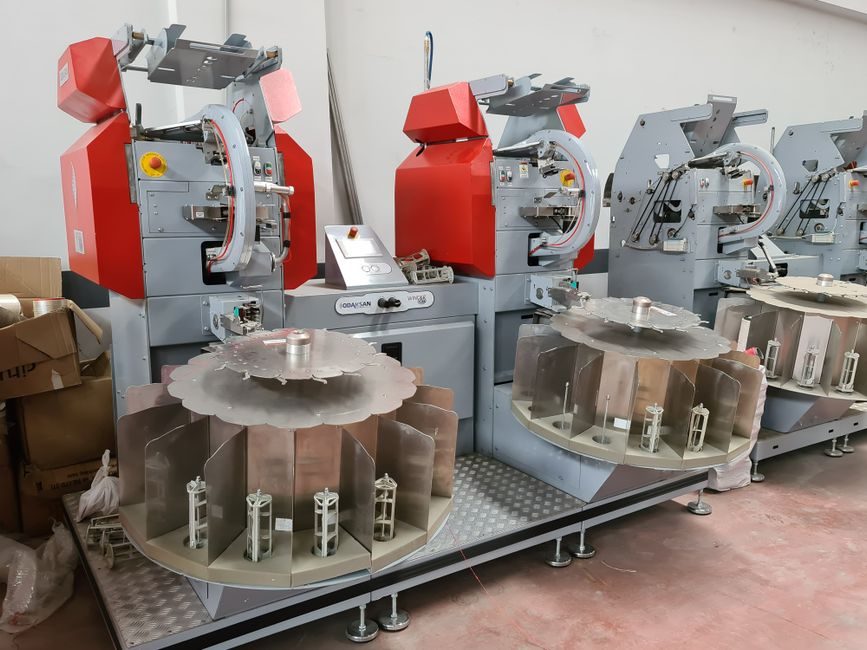
Shrink wrapping machine selection hinges on four decision variables: throughput range (5-180 p/min across current 2026 OEM catalogues), pack architecture (seal-bar vs shrink-tunnel), container substrate, and film compatibility. Match the wrapper class to product geometry before chasing speed.

A standard 12"x12"x12" ECT-32 single-wall corrugated carton retails at $70.67 for a 25-pack on eBay as of July 2026, while a 12"x12"x12" industrial spec sits between $48.82 and $70.67 per 25-count pack depending on seller and flute option.
Industrial dust collector system prices on Made-in-China.com range from about US$1,999 to US$40,000 per piece MOQ in 2026, with cement-plant baghouse units clustering US$3,000-US$7,999 and laser-fume extractors around US$6,800-US$7,000, while conventional filter units still dominate 85-90% of instal

New 55-gallon steel drums list around USD 95-180 on Alibaba bulk listings while used steel barrels sit at USD 45-85 and food-grade plastic drums run USD 80-130, with total cost-of-ownership shifting sharply by UN rating, gasket spec and heater/dolly add-ons.
A 55-gallon drum is not one size: steel closed-head measures 33" tall x 23" dia, open-head 34-3/4" x 24-1/2"; HDPE plastic and fiber variants shift another 1-2". Match material, head style, UN/UL rating and tare weight to the liquid or solid being stored.

Cardboard tube pricing in 2026 splits three ways: sub-$0.15 industrial cores from China, US$0.50–10.00 branded gift/cosmetic tubes at 500-MOQ, and UK/EU bespoke postal/composite tubes priced per quote. Material, MOQ and wall construction drive 80% of the spread.

Cardboard tube selection is driven by five engineering variables: inside diameter (ID), wall thickness/ply, length tolerance, end-closure style, and intended load — postal tubes, industrial cores, piling tubes, display tubes and void formers each pull those variables in different directions, so matc

Industrial baler machines list between US$20,000 and US$83,333 per set on Made-in-China.com (July 2026 listings); horizontal hydraulic and PET-bottle presses dominate export catalogs from Nantong and Jiangsu factories.

Vertical balers suit sub-2 t/h cardboard and plastic streams below 60 kN ram force, while horizontal two-ram and channel balers handle 5-20 t/h paper, RDF, and scrap-metal feeds at 800-3000 kN. Match machine class to material bulk density, bale target weight, and tie method before comparing hydrauli

Robot palletizers dominate 2026 end-of-line capex with US$12,000–78,000 entry pricing, throughputs of 3,600–36,000 units/h, and payloads from 20–450 kg across food, beverage and chemical plants.
Chamber (bell-type tabletop) vacuum packaging machines at 65 packs/hour throughput in 8 mm-seal-bar AISI-304 stainless builds dominate 2026 spec sheets; select by chamber geometry, MAP option and pump brand rather than nameplate throughput alone.

Entry-level manual carton sealers ship from Chinese factories at roughly US$0.10–1.50 per piece for OEM tape-and-glue components, while automatic case erectors and high-speed servo top-and-bottom sealers cluster in the US$3,000–12,000 band and full four-corner sealers from audited Diamond suppliers
Carton sealing machine selection in 2026 hinges on four decisions: tape vs hot-melt, manual vs automatic, uniform vs random-size, and machine speed matched to upstream case erector throughput. Buyers should size by carton L×W×H range, case erector output, and tape-head cycle rate before comparing pr

Selecting a coding machine for aerospace part traceability hinges on 0.1 mm-resolution CIJ/TIO2 ink on Ti-6Al-4V and Inconel 718, AS9100D-compliant data capture, and DOD ink-jet fallback for curved or low-flatness surfaces per OEM 2026 guidance.

Coding machines for industrial lines divide into inkjet, laser, TIJ, CIJ and pad/screen variants, with selection driven by substrate, line speed, code durability and IP/NEMA rating. China OEM cluster in 2026 lists CO2 laser fly-line units at US$2,000-5,000 FOB tier and continuous inkjet stainless un
China dominates strapping machine OEM supply with 1,832+ Alibaba listings and 2,022 Made-in-China catalog records as of 2026-07-10; entry-level PE banders sit at US$2,000-2,500, while premium rotary carton lines from Guangdong reach US$100,000-2,000,000.

Strapping machine sizing starts from three load facts — package weight, bundle dimensions, and daily throughput — which set strap width, tension range and automation tier. PP and PET are the dominant band types, with cycle speeds from 17 straps/min on bench units to 60+ on inline systems.
Marine cargo lashing demands corrosion-resistant strapping machines using stainless/polymer-clad frames, PET or woven polypropylene strapping band rated for salt exposure, and 400-800 N seal tension for container breakbulk and offshore pallet loads.

China dominates the wrapping-machine supply base with hundreds of B2B-listed vendors clustered in Jiangsu, Shanghai, and Zhejiang; the brightest competitive levers buyers weigh are throughput, automation grade, and after-sales footprint.

Sizing a wrapping machine comes down to four numbers: package L×W×H, throughput in packs/min, film type (PE stretch, BOPP, flow-wrap PE) and turntable/ring diameter. Match those before you quote options, not after.

For HVAC wrapping, a horizontal orbital stretch wrapper handling profile lengths 1.5–6 m at 30–60 rpm is the spec that actually fits coils, duct sections, and packaged AHUs without rework.
An order picker is a low-level order picking truck designed for warehouse SKU retrieval at the first and second picking levels, lifting operators to heights of roughly 2.4–12 m, with load capacities from 90 kg to 1,500 kg depending on configuration.

Indoor and warehouse reach-truck sourcing concentrates in China (Anhui HeLi, Noblelift, Zowell, Jialift, Hangcha) and Europe (Linde, Cat, CLARK, Aisle-Master), with 2026 listing directories indexing 25+ makers and roughly 130 SKU-level entries.

Specifying a reach truck for chemical processing requires ATEX/IECEx Zone 1–2 rated units, stainless or corrosion-protected chassis, and 1,400–2,500 kg load bands to meet hazardous-area safety mandates and corrosive-ambient duty cycles.

Sizing a dock leveler starts with four numbers — capacity (6,000-100,000 lb), deck length (6-12 ft), pit width, and truck-bed height band — then matches lift mechanism (hydraulic, air-powered, mechanical) to duty cycle.

Platform trolley sourcing in 2026 is split between ~30 European specialist makers (FlexQube 15 listings, Handle-iT 12) on DirectIndustry and a price-aggressive China cluster led by Hebei/Zhejiang factories such as Century Langyi (FOB US$12-16/100 pcs MOQ) and J and K Industrial (US$10.08-31.98/100 p

Selecting a platform trolley for power generation hinges on load class, deck material, and rail/lock-down hardware, with 500-2000 kg SWL steel-deck units dominating outage and turbine-hall work. Stainless and aluminum decks are specified for clean-room or hydrogen-area zones, while fold-flat carts s

Hebei-led Chinese manual pallet jack makers cluster around three price bands: US$73-75 entry-level, US$82-110 mid-range, and US$110-120 stainless/portable models, with 2-10 piece MOQs dominating Alibaba and Made-in-China listings.
Manual pallet jack sizing hinges on three load-bearing decisions: rated capacity (2,000-5,500 lb / 1-2.5 t standard, 3 t / 6,600 lb being the dominant export SKU), fork length matching pallet stringer length, and fork spread matching pallet entry width.

For automotive assembly and parts-plant duty, the best manual pallet jack is a 5500 lb (≈2,500 kg) standard-duty truck with 48" × 27" forks, polyurethane steer and load wheels, and a chrome-moly pump; alternatives in the 5,500–6,600 lb band cover 80% of line-side needs.
China-origin pallet stacker suppliers cluster in Jiangsu and Anhui with FOB price bands US$780-5,500 across manual, semi-electric and 1.5-2 tonne full-electric models; manual units dominate entry pricing while battery/electric stackers carry the spec ceiling.
Pallet stacker sizing hinges on four inputs — load, lift height, aisle width and power class — with 1000–2000 kg walkie and 1200–3500 kg ride-on units dominating mid-2026 SKU lists from TCM, Niuli, EBILTECH and PalletMaster Finland.

Semiconductor fabs and back-end OSAT lines typically need pallet stackers with stainless or ESD-coated components, IP54+ enclosures, food-grade hydraulic oil, and cleanroom-suitable lifting geometry in the 1,000-2,000 kg load class.
A pallet stacker is a walk-behind or ride-on wheeled loader that lifts a palletized load vertically on fixed forks for stacking into rack bays or order staging, distinct from a forklift by its compact footprint and lower top speed. Selection pivots on load capacity 1,000-3,500 lb, lift height 8-20 f

China-based electric pallet truck makers dominate the 2026 supplier map, with FOB price bands of US$400–1,260 for 1–3 ton Li-ion / lead-acid walkie units, monthly line capacities of 1,500 units typical, and 500 mm standard load centres for the 1–5 t class.

Food and beverage electric pallet trucks in 2026 sit in a 1500-2500 kg load class with stainless or food-grade epoxy chassis, IP54-IP65 drive electronics, and cold-store ratings down to -25C; HF walk-behind units such as the ICEM 2000 kg model anchor the spec band for general dry-area handling.

Electric pallet trucks in 2026 span 1,400–3,000 kg load classes, 24 V or 48 V lithium systems, walk-behind/platform/stand-on operator formats, and require matching tiller type, fork geometry and battery spec to aisle width, run length and duty cycle.

AS/RS unit-cost bands on Made-in-China.com cluster around US$180-200 per piece for shuttle-pallet builds with 10-piece MOQ, while unit-load stacker-crane cells from Jiangsu and Anhui makers dominate the supplier map entering July 2026.

AS/RS sizing turns on SKU count, throughput order-lines per hour, and storage envelope height. Unit-load mini-load and shuttle systems cover 60-80% of new mid-size builds, with tote stack height typically 6-12 m.

For pharmaceutical AS/RS in 2026, unit-load or mini-load systems with GMP-grade stainless extractors, ISO 14644-7 cleanroom compatibility, and 21 CFR Part 11 electronic batch records are the dominant spec; cold-chain and controlled-substance vaults add -20 °C and DEA-compliant sealed-bin requirement
Qingdao Palet Machinery, Conovey, Affeldt Fördertechnik and HuaWei Silkroad are active conveyor sorting line suppliers as of July 2026, with adjustable-incline belt conveyor FOB bands of US$3,200-4,000 from Made-in-China listings and 32+ adjustable-slope product variants tracked on DirectIndustry.

Sorting conveyor line selection hinges on matching throughput (cases/hour), package size envelope, belt/roller type, drive specs, and divert strategy to the SKU mix; lined up against these criteria, belt vs roller vs cross-belt sorter choices split clearly on flexibility, noise, and cost.

Vertical lift module (VLM) suppliers cluster in two camps: European-originated OEMs (Modula, Kardex, SSI Schaefer) with WMS/AMR integration stacks, and China-based lifting-platform makers (e.g. Eterlift) scaling scissor-lift and freight-lift variants. The VLM market reached US$ 950.19M in 2024 and i
Vertical lift modules (VLMs) in pulp and paper mills cut pick-area floor space 75-90% versus static shelving, but selection hinges on load class, tray footprint and dust/lint tolerance, not brand. For spare-parts and consumables SKU storage, a 500-1,000 kg/tray unit with galvanized trays and a 7-12
A Vertical Lift Module (VLM) trades floor area for height: two columns of trays served by an extractor that delivers the right tray to an operator window in 10–20 seconds, freeing 60–85% floor space over static shelving.

Autonomous Mobile Robot (AMR) supply landscape: 7 dedicated industrial manufacturers list AMRs on DirectIndustry, while China's AMR market is projected to hit $14.4B by 2030 at 21.4% CAGR, reshaping buyer choice across payload and SLAM tiers.

Choosing an Autonomous Mobile Robot in 2026 hinges on matching payload, navigation method, fleet software and safety certification to the actual route and SKU profile — ROS 2-based platforms, 2D SLAM laser, QR/AR-code floor tape and AMR-to-WMS APIs are the four levers a spec engineer must hold firm

China dominates pallet rack supply with 30-piece MOQs and teardrop frames from US$80/sqm, while UK RediRack sells site-surveyed EN-standard systems; selection pivots on beam capacity, fork clearance and seismic code, not sticker price.
Pallet rack sizing starts with three measured inputs — pallet footprint, unit load weight, and clear-ceiling height — and resolves into a beam/frame/anchor configuration governed by RMI MH16.1 and CSA A344 for North American builds.
Heavy-duty selective pallet rack with 2000 kg/level capacity and 75 mm adjustable beam pitch is the baseline for HVAC parts storage, sized at roughly L2300 × W1000 × H5025 mm per bay in 4 levels. Cantilever and drive-in variants handle long trunk duct and coils.

Pallet rack selection hinges on matching frame capacity, beam load, pallet type and fork-truck aisle width to your SKU and throughput. Teardrop selective racking still dominates US warehouses, with roll-formed and structural columns competing on cost vs impact tolerance.

Stacker crane selection is driven by load capacity, lift height, aisle width, and warehouse duty class; miniload units with photoelectric positioning sensors suit bins under 100 kg in food, pharma, and tobacco storage.
Vibrating conveyor sourcing in 2026 splits cleanly into three supply tiers: European specialty OEMs for sanitary and high-tonnage duty, North American integrators for alignment/feeding, and a large Chinese long-tail of 2,000+ electric-vibrator and shaker-tray makers with MOQ floors as low as one pie
Choosing a vibrating conveyor hinges on matching drive type (electromagnetic vs eccentric-motor), trough geometry, material of construction, and bulk-product behaviour to the duty cycle, with capacity figures typically ranging 1–500 t/h depending on trough width and drive class.

Global pneumatic conveying system supplier base spans 9 OEMs in Europe plus dense China and India clusters offering dense-phase, lean-phase and central-vacuum units, with conveying distance ratings up to 2000 m and line sizes DN50-DN300 as the dominant spec bands.

Pneumatic conveying selection starts with phase mode (dilute vs dense vs semi-dense), then is constrained by solids-to-air mass ratio, particle size/De, distance/turn count, and material abrasiveness/corrosion class; Air-Tec and ANDE list 14 OEM systems on DirectIndustry.
For 2026 power-generation projects, dilute-phase positive-pressure pneumatic conveying is the default choice for dry fly ash, FGD gypsum and pulverised fuel below 30 t/h, with dense-phase units reserved for abrasive or friable materials.
Vertical bucket elevator line cards in July 2026 list 23 manufacturers and 28 products on DirectIndustry, dominated by BEUMER, FEECO, Cimbria and Cidiesse; China clusters on Made-in-China and Alibaba supply cement, clinker and feed units from US$10M–US$50M factories.

Bucket elevator sizing hinges on throughput (25–1200 tph), lift height, bulk density and bucket spacing; centrifugal units cover fine/granular free-flowing product up to ~100 m, while continuous/discharge types handle abrasive, large-lump or hot duties.

For automotive plants, centrifugal discharge belt-bucket elevators with mild-steel AA-type or HD continuous buckets running at 1.0-1.5 m/s on PVC or rubber belts cover most stamping scrap and weld-cell return applications under 30 m lift. For hot sintered parts above 150 °C or abrasive shot, switch
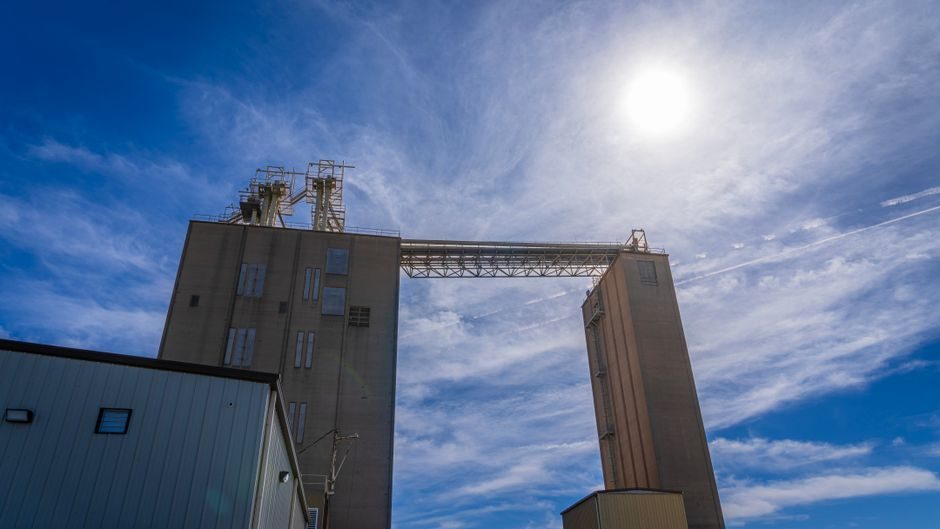
Bucket elevator selection hinges on matching four hard gates — material class, lift height, capacity, and duty environment — before comparing centrifugal vs continuous vs positive-discharge types on chain or belt.

Global overhead conveyor sourcing in mid-2026 spans North American OEM Bridgeveyor C-250, Indian integrators like Raj/Advance, and a deep China cluster offering overhead chain conveyors from US$480-680/meter MOQ 1 m on Made-in-China.com. Selection hinges on payload, accumulation, and standard compli
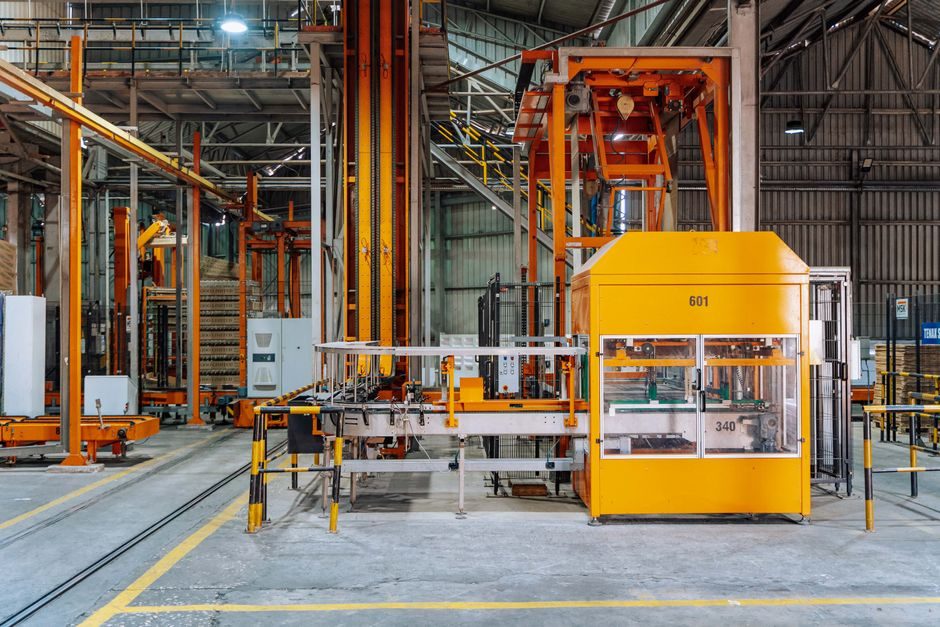
Overhead conveyor sizing hinges on per-load mass, chain pitch, path geometry and accumulation duty; DirectIndustry lists 12 transport-classified OEM systems, while Bridgeveyor's C-250 line defines a North-American baseline of 250 lb per carrier capacity.

Overhead conveyors for semiconductor fabs are specified as enclosed track, cleanroom-rated power-and-free or monorail systems; the 2026 buildout favors ESD-safe chain, vibration <0.5 g and ISO Class 5 compatibility.

Mesh belt conveyor supply in mid-2026 remains heavily concentrated in Chinese OEM clusters, with Jiangsu and Hebei factories dominating stainless steel wire belts, PTFE-coated mesh, and flat flex constructions at FOB unit prices spanning roughly US$4 to US$500.

Sizing a mesh belt conveyor starts with four hard gates: belt width (typical 1,500 mm production max), wire diameter (0.8–6.0 mm), mesh opening/open area (≤60% on fabric belts), and the temperature/chemistry of the product being carried.
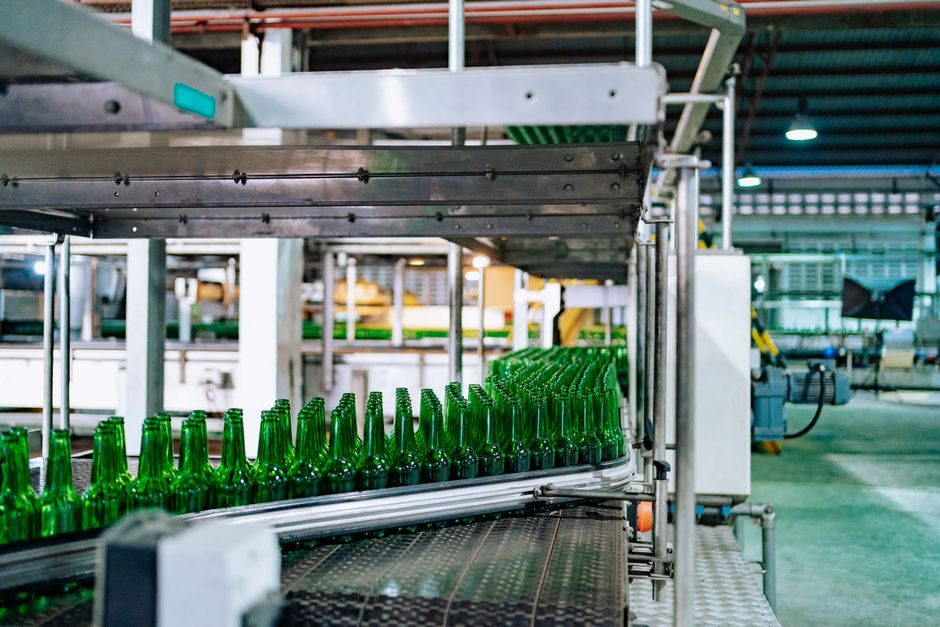
Food-grade mesh belt conveyors split into stainless steel woven mesh for high-temp wash-down and modular plastic spiral-rod for fast changeover. Selection gates: 304 vs 316L material, belt pitch, FDA/EU contact compliance, and drive duty cycle.

A mesh belt conveyor is selected by four hard gates — operating temperature, product loading per square metre, belt material grade, and drive/span geometry — and ignoring any one of them is the single most common reason a line is re-engineered within 18 months of start-up.

Chain conveyor sourcing has consolidated into two lanes by 2026-07-05: European OEMs selling engineered chain-drive systems on DirectIndustry (18 chain-tagged suppliers) and Chinese factories on Alibaba/Made-in-China/Okn

Chain conveyor sizing and selection starts with payload per meter, chain pitch, and bend geometry: a horizontal 6.0HD-style indexer handles indexing accuracy at 6-inch link length, while modular GKF builds flex for assembly, and TH-class vertical units lift bulk materials. Match chain, drive, and fr
Stainless 304/316 chain conveyors with FDA-accepted UHMW or thermoplastic link surfaces, IP65 enclosures, and tool-less disassembly dominate pharmaceutical lines, with 72 vendors and 171 product listings catalogued on DirectIndustry for pharma duty.

Screw conveyor sizing ties to four hard numbers: trough diameter, rotational RPM, material density, and angle of incline. Pitch, flights, and hanger-bearing placement move with those four; CEMA 300/352 and the 2026 vendor feed define the selection gates.
Screw conveyors move 10–7,500 cu ft/hr of bulk material on a rotating helical flight, with selection driven by material class, capacity, incline angle, and shaft vs. shaftless design.

Roller conveyor sourcing in 2026 splits into three drive families — gravity, line-shaft/chain-driven (O-ring belt) and motorised MDR/24V DC rollers — each pinned to load, curve and zone-control needs. DirectIndustry indexes 225 manufacturers and 581 product entries for the category, and active

Roller conveyor sizing starts with three numbers — load per roller, roller diameter and centre distance — which together set frame gauge, axle size and drive type. Live-load capacities on standard gravity sections run from 100 kg on light modular lines to 1,180 lb on 18" × 10' heavy-duty frames.

Roller conveyors for oil and gas must combine 304/316 stainless construction, ATEX/IECEx-rated motors and sealed bearings rated for sour-service H2S exposure. Gravity, powered and skatewheel variants each map to different zone-1/zone-2 handling duties from tubing yards to modular skids.
Roller conveyor selection starts with four gates: load per roller, total live load, roller diameter/spacing, and drive method. Match gravity vs powered, then frame/roller material, then options. Skip if you need inclines above ~5° or sanitary washdown without redesign.
China supplies the bulk of low-cost belt conveyor systems, with TD75 and TDII fixed-frame models, incline units, and vulcanizer splicing tooling clustering around US$3,800–6,600 FOB; the buyer trade-off is unit price vs verified QA, belt spec and after-sales support.
Belt conveyor selection is governed by four hard gates — material profile, belt type, length/width envelope and drive layout — applied before any brand shortlist. Misalignment on the first gate alone flips a $5k unit into a $50k retrofit, so spec the load first.
Plastic pallet specification in 2026 hinges on four binding decisions: HDPE vs PP, one-way export vs pooled returnable, rackable static load, and footprint. China FOB bands sit at US$3-30 per piece (MOQ 10), with 1200x1000mm blow-molded units at US$10-15 and heavier 1690x1010mm 6t versions at US$26.
FIBC bulk bag selection hinges on five design factors: safe working load (SWL) typically 500–1500 kg, safety factor 5:1 or 6:1, UN-certified fabric weight 140–220 g/m², electrostatic classification A/B/C/D, and food-grade or pharma-grade liner compatibility per application.
Injection-moulded PP turnover boxes in the 60–100 L class are quoted from US$2.00 per piece at 100-piece MOQ on China B2B platforms as of 31 May 2026, with production lines rated 10,000 pieces/month and HS code 3923 10 00.0 for push-up logistics turnover boxes.
Corrugated carton boxes typically handle 5–25 kg unit loads with single-trip retail handling, while FIBC bulk bags move 500–1500 kg in a single woven PP lift for dry bulk; the two occupy different cost-per-ton and stacking tiers and rarely substitute directly.

LLDPE stretch film spot prices on major B2B platforms cluster around US$1.00–2.00/kg for bulk machine and hand grades as of 2026-07-04, with hand-roll 1-roll MOQ lots trading US$59–199 and 12–50 µm gauges dominating the SKU matrix.
Industrial bench scales in 2026 segment by capacity band (3–600 kg), resolution class (0.01 g to 1 g) and IP rating; barcode-integrated and hygienic bakery models now drive most new line-spec purchases per METTLER TOLEDO industrial guidance.
For 2026 reach truck buying, a 1,200-2,000 kg electric stand-up or seated reach truck with 7,000-12,000 mm lift and 1,000-1,270 mm chassis is the narrow-aisle baseline. FOB China price band sits at US$6,000-18,500 per unit; 1.0-1.4 t Hyster R1.0-1.4E and CESAB R100 anchor European spec.
Chinese AGV market hit 9.5B CNY in 2024 with 27.5% four-year CAGR, KIVA-class units over 60% share; new AGV robot pricing spans 80k-800k CNY by navigation and load class.

FOB FIBC bulk bag pricing on major Asia-based B2B portals sits at roughly US $3–10 per piece for standard 1,000-piece MOQs as of 2026-06-29, with baffle, sift-proof and Type D conductive variants commanding the upper end of that band. Real landed cost is driven by fabric weight, SWL, l

FIBC bulk bags in 2026 price between US$1.78 and US$5.6 per piece FOB China at 200-2000-piece MOQs, with PP woven 1000 kg super sacks dominating cement, chemical, fertilizer and mineral applications.
Turnover boxes in 2026 are dominated by injection-moulded PP and HDPE, with 25-60 L capacities, 5-30 kg load ratings and 1,000-5,000 piece MOQs prevailing on Alibaba and Made-in-China listings.

Plastic pallet prices span US$75 entry HDPE sleeve boxes to US$400+ rigid HDPE export units; size, material grade, dynamic load, and runner config drive 70% of cost variance.
Industrial bench scales from Chinese vendors span roughly USD 90-1,700 per unit on B2B portals as of 2026-07-04; mild-steel washdown units sit at the low end while 0.1 mg semi-micro analytical balances top the range, with METTLER TOLEDO precision SKUs in the mid-band.

Checkweigher selection reduces to six binding spec gates — throughput, product weight range, accuracy class, belt width, environment/IP rating, and integration protocol — applied before any vendor brand comparison.
Labeling machines and strapping machines serve distinct packaging-line functions; current China export listings price a flat-bottle labeller at US$2,999–3,800/piece and corner-label sealers at US$5,900–6,500/piece, while automatic strapping units share many of the same vendors' catalogues alongside

Light-duty steel platform trolleys sit in a €80–€250 ex-works band in 2026, with verified European list pricing at €110 for an 800 kg workshop unit (Kstools 800.0015) and Asia-sourced OEM hand-truck quotes around US$79–$150 FOB at single-pallet MOQ.
AS/RS unit-load mini-load and vertical-lift module pricing in 2026 typically runs USD 35,000-300,000 per aisle, with high-bay pallet stacker cranes at USD 150,000-600,000 each and full turnkey projects between USD 1.5M-20M depending on height, payload and WMS/WCS integration depth.

Pallet rack buying in mid-2026: selective racking sits at US$50-380 per set, push-back at US$0.85-1.20/set, mezzanine kits US$260-304, with lead-time and load-class now the decisive spec, not headline price.

Teardrop-style selective pallet rack remains the default spec for U.S. and European warehouses, with new uprights shipping in 48 hours and used systems available from long-established distributors; capacity ratings, beam-to-upright connection, and RMI/EN 15635 compliance drive selection.
ASRS stacker cranes on Made-in-China list at US$20,000–US$200,000 per unit (June 2026 listings), with mini self-lifting stackers starting at US$1,499 FOB. Real project cost is dominated by height, payload, aisle width and WMS/WCS integration, not the bare crane.

Vibrating conveyors span $8,000 for a basic 2m trough unit to over $250,000 for a tall spiral or sanitary cooling unit, with material (304/316L), drive (electromagnetic vs unbalanced-motor) and elevation driving most of the variance.

Mesh-belt conveyors and vibrating conveyors solve the same bulk-handling problem from opposite directions: a continuous positive-drive woven steel belt versus a resonance-driven trough, and the spec levers (drive type, temperature, hygiene, length) decide which one wins a given line.

A turnkey dilute-phase pneumatic conveying line for under 5 t/h typically lands between USD 80,000 and USD 350,000 in 2026, while dense-phase packages for abrasive or friable materials run USD 250,000 to USD 1,200,000+ depending on distance, bends, and gas-source choice.

Pneumatic conveying and chain conveyor move bulk solids on fundamentally different principles — air-suspended particle flow vs positive- or friction-driven mechanical pull. Pneumatic systems suit fine, dry, abrasive powders at rates of a few hundred kg/h up to ~30 t/h per conveying line; chain conve

Pneumatic conveying system selection is driven by six engineering criteria: material bulk density, particle size distribution, conveying distance, capacity in t/h, pressure profile (positive-pressure vs vacuum), and phase (dilute-phase vs dense-phase). Mismatching any one criterion to material behav
HDTD centrifugal bucket elevators from Hebei Africa Machinery list 0.27–5.81 m³ bucket volumes with capacities 1.5–134 m³/h across 7 model sizes, FOB bands roughly $1,800–$24,000 on Alibaba-track data.
A 2026 bucket elevator is a vertical bulk-material conveyor rated for up to ≤55 mm feed, ≤50 m lift and 34–1112 m³/h capacity; selection is driven by particle size, height, casing seal and material, not by rpm.

Mesh belt conveyors carry product on a woven or spiral metal wire surface; standard belt conveyors carry it on a continuous elastomer or PVC/PVG/PU belt. Mesh belts handle heat, drainage, and oil-quench duty; standard belts win on long centres, lower mass, and lower capital cost per metre.
Roller conveyors move unit loads horizontally on gravity- or motor-driven tubes; bucket elevators lift bulk solids vertically on belts or chains. Pick roller for cartons/pallets, bucket for grain/cement/feed. Spec overlap is narrow — wrong choice doubles energy use or blocks throughput.
Storage cage pricing in 2026 runs roughly $30–$180 for light-duty folding wire mesh, $80–$260 for stackable stillages, and $200–$650 for heavy-duty pallet-cage systems on Made-in-China listings; total landed cost is dominated by wire diameter, mesh aperture, surface finish, and MOQ tier.
Foldable welded wire mesh storage cages in the 1000x800x800 mm class typically run US$19.90-90.00 per piece FOB China at 5-100 unit MOQs, with 800-1000 kg load ratings and 50x50 mm mesh on 6 mm wire. Lead times, stackability and finish separate usable warehouse cages from throwaway imports.
New 1000L HDPE IBC totes ship in a $68-85 FOB China band per piece at 42-piece MOQ, while UN-rated stainless steel 1000L IBCs range $1,000-1,650 per piece; 20' ISO tank containers sit at $11,000-15,800. Material and certification drive a 15-20x price spread.
IBC tanks and storage cages serve different bulk-handling jobs: a 1,000 L IBC (PE inner bottle + steel cage + pallet) is a UN-certified liquid container, while a wire-mesh or welded-steel storage cage is a dry-goods stackable stillage. Selection hinges on product state (liquid vs solid), UN/UN-relat
A 1000 L plastic IBC tank ships FOB US$90-120 per piece from Chinese suppliers as of 2026-05, with stainless 304/316 variants tracking roughly 3-5x higher; spec the frame, valve and UN rating before chasing the headline price.
FIBC bulk bags ship at roughly US $2.50-10 per piece at 1,000-piece MOQ while stainless-frame IBC tanks sit an order of magnitude higher; choice hinges on payload, reuse cycles and containment duty rather than headline price.
Corrugated carton box FOB bands in mid-2026 run US$0.05–0.45 per unit on Alibaba-style B2B listings, with kraft and B-flute dominating spec sheets and ECT/Mullen ratings as the decisive cost drivers. Carton erecting machines sit at US$28,000 per piece MOQ-1.
Filling machine selection hinges on product state (liquid, paste, solid), accuracy tier (±0.5-1.0% for liquid, ±0.1-0.3 g for solid), contact-material compatibility (316L SS, PTFE seals), and throughput; matching these four gates first prevents 80% of spec churn seen in 2026 procurement cycles.
Spec-driven filling machine buying 2026: 385 vendors, 1,433 models on DirectIndustry, with liquid models spanning US$2,599 piston units to US$200,000 turnkey beverage lines and sterile RTU syringe systems at US$52,000-81,000.
Belt conveyors and overhead conveyors serve overlapping but distinct transport duties; belt systems dominate long-run, high-tonnage horizontal or inclined bulk movement, while overhead systems win where floor space, return loops, or paint/surface-treatment in-line access dictate.
Stretch film 2026 buying hinges on five hard spec gates: thickness 17-30 µm typical, LLDPE resin base, pre-stretch ratio 200-300%, hand vs machine grade, and pallet format fit. Source pricing July 2026 runs $1.10-1.50/kg on 500 kg MOQ for cast LLDPE.
Mesh belt conveyor prices span roughly $65-70 per meter for Chinese-made metal mesh belts on FOB terms (June 2026), while stainless steel woven belts and high-temperature furnace belts are quoted per square meter or per project. Total installed cost is driven by belt material, drive system, and furn
Selective pallet rack frames list at US$0.80–1.10/kg MOQ 100 kg on Made-in-China, with full bay assemblies US$25.50–34.50/set MOQ 5 and heavy-duty frames at US$80.00/sq ft; standard upright sizes 90×70mm to 120×95mm with 75mm beam adjustability dominate 2026 pricing.
Vertical Lift Modules (VLMs) compress storage footprint 80–85% versus static shelving and cut picker travel to roughly 1 metre, with the 2024 VLM market valued at US$ 950.19 M and tracked to US$ 1,766.08 M by 2031. Selection pivots on tray payload, usable height, throughput class, software/ERP
Conveyor sorting line buying in 2026 hinges on three numbers — throughput (parcels/hr), induction footprint, and chute/diverter count — with 8 manufacturers globally shipping case and box sorters at US$50–269/meter for belt sections.
Roller conveyor selection reduces to six gates: load per roller, roller diameter/pitch, drive type (gravity/slip-on/chain/belt), material (steel/PVC/aluminium), environment, and frame profile. Spec the gates in that order.
AMR (Autonomous Mobile Robot) and stacker crane solve different intralogistics problems: AMRs navigate freely via SLAM-based localization on the warehouse floor with payloads typically 50–1500 kg, while stacker cranes run on fixed rails/aisles in AS/RS with lifts to 12 m and throughputs of 20–60 cyc
Strapping machine selection hinges on four gates: strap material (PP vs PET vs steel), throughput (straps/min), bundle geometry, and seal method (heat-weld vs buckle). Semi-auto units hit 17 straps/min; automatic lines scale into pallet-line duty.
An AS/RS system in 2026 is a computer-controlled stacker-crane + rack installation that runs put-away and retrieval without manual travel, and the right class depends on unit-load weight, throughput and ceiling height — not on marketing claims.
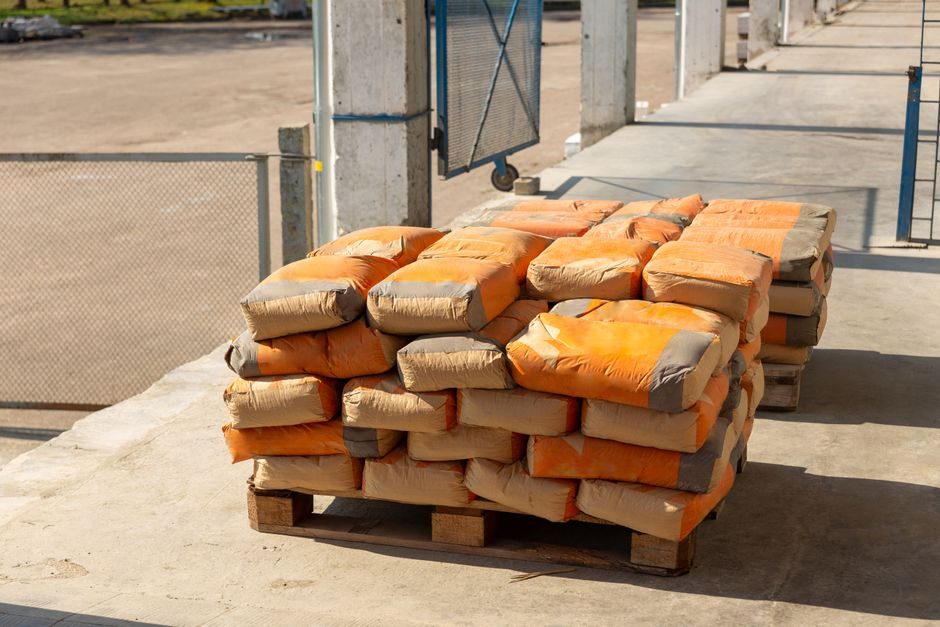
Manual pallet jacks priced at US$65-120 per unit and 2-3 t electric pallet trucks at US$580 on Made-in-China 2026 listings; selection turns on daily shift volume, travel distance, load class, and aisle width, not sticker price.
Wrapping machines enclose a single product or bundle in film, paper, or shrink film at 30-200 packs/min; case packers collate counted products into an RSC or wrap-around case at 5-30 cases/min. Pick the wrapper when the unit is the shipper; pick the case packer when units must be grouped, oriented,
Belt conveyor selection hinges on matching load profile, environment, and belt type — flat, ribbed, or timing — to duty cycle, with idlers, pulleys, and guarding sized to material and code.
AMR selection on 2026-06-25 hinges on five gates: payload × reach, navigation stack (SLAM vs line-follow), fleet manager openness, safety rating per ISO 3691-4, and floor-condition tolerance. Get any one wrong and the deployment slips from weeks to quarters.
Industrial coding machine prices in mid-2026 span US$90 handheld inkjet units to over US$50,000 CIJ lines, with the dominant cost levers being print technology, line speed, ink chemistry and the number of print heads.
Belt conveyor selection in 2026 hinges on belt type, load class, incline angle, and duty cycle. DirectIndustry lists 511 manufacturers and 1,218 products; Interroll BM 8360 carries 20 kg at 0.5 m/s; Vanguard B-series delivers 60-1427 t/h on 4-37 kW drives.
Stacker cranes store and retrieve unit loads in fixed-aisle racking; sorting systems route items across a conveyor network for order fulfillment. They are not interchangeable — one is a storage/retrieval machine, the other a flow-routing system.
Hand vs machine-grade stretch film splits on 4 specs: thickness (17-35 µm), pre-stretch (up to 300%), cling side count (single/double), and roll core ID (50/76 mm). LLDPE is the dominant resin; 5-7 layer coex lines now standard for high-performance pallet wrap.
Carton erecting machines in 2026 span 15-180 pcs/min output, with PLC-controlled automatic case erectors priced US$3,500-6,000 FOB China, selection pivoting on box size, run length and integration scope.
Wrapping machine selection is driven by four hard gates — product geometry, throughput in packs/min, film/format type, and hygienic duty class. Match those before brand, price, or automation level. This guide maps gates to machine families, standards, and verifiable use cases through June 2026.
AS/RS and Vertical Lift Module (VLM) solve the same problem from opposite directions: AS/RS scales by building wider and taller in standard footprints, while a VLM condenses the same SKU count into a 25-40% smaller floor box with a 2-3x pick-rate multiplier. VLM market tracked from US$ 950.19 M in 2
Platform trolleys move 300-2,000 kg loads at floor level with no lift, while electric pallet stackers lift 1,500-2,000 kg to 3.0-5.4 m on a 24 V mast. Choose a trolley for short push-only routes; pick a stacker when pallets must be placed on racking above knee height.
Automatic shrink wrapping machines span roughly US$10,000 to US$105,000 per set on Chinese export listings as of 2026-05/06, with a low-cost manual-band around US$15,000-60,000 (Jiangsu) and a high-end flow packer class at US$63,000-105,000 (E-Star) and US$71,000-73,000 (Y.C.T.D.).
Plastic pallet selection on 2026-07-01 hinges on five spec gates — load class, moulding process, deck style, racking duty and hygiene-grade material — backed by ISO 8611, FEM 9.832 and food-contact FDA/EU rules.
Industrial wrapping machines in mid-2026 split into turntable, orbital, shrink, and tape-wrapping families, with pallet turntable units at US$2,300–7,800 and automatic cable tapers starting near US$700 per recent China export listings.
New wrapping machines for industrial lines range from US$700 for a desk-type tape wrapper to US$60,000+ for a full-automatic PE shrink wrapper as of June 2026 sourcing data; the 4-7x spread tracks automation, throughput and film/spec scope, not just build quality.
Shrink wrapping machine selection in 2026 is decided by film type (PE vs polyolefin vs PVC), throughput, pack geometry and tunnel temperature control; chamber units suit low-volume shops, while L-bar, side-seal and continuous-motion wrappers cover 30 to 200+ packs per minute.
Conveyor sorting line price in mid-2026 ranges from roughly USD 6,500 for a single-belt parcel scanner unit to USD 120,000+ for a cross-belt sorter, with most industrial turnkey installations landing between USD 80,000 and USD 350,000 depending on throughput, diverters and controls.
FOB factory prices for entry-level fully automatic capping and sealing machines sit at roughly US$19,000-21,000 per set on Chinese B2B portals in 2026, while high-end oral-liquid tube-filling-and-sealing lines with cartoning list at US$35,000-42,000 per set.
Industrial sorting system selection in 2026 is driven by six engineering gates — item profile, throughput, accuracy, footprint, integration, and lifecycle cost — with cross-belt, tilt-tray, shoe, and induction loop variants matched to specific parcel/case/bulk ranges.
Shuttle system selection hinges on five gates: SKU count, throughput per aisle, ceiling height, fire-code class, and shuttle-versus-crane trade-off. Pick the wrong gate and you overpay 30-50% or strand throughput.
Shrink wrapping machines in 2026 span three core architectures — manual chamber, semi-automatic L-bar sealer, and fully-automatic flow wrappers — with Chinese OEM listed pricing for full automatic carbonated-drink systems at US$71,000–73,000 per set MOQ 1 as of May 2026. The right pick is drive
Screw conveyor prices in 2026 span roughly $1,200 to $36,000 per set on Made-in-China, with US directindustry listings and EU OEMs sitting higher. Real cost is driven by trough size, flight type, material, drive, and sealing — not headline list price.
Industrial labeling machines on the China B2B market span US$1,000 to US$28,936 FOB as of 2026-05 listings, with price driven by automation level, label head count, and throughput, not by brand prestige. Buyers should anchor selection to spec gates first, then negotiate volume tiers.

Plastic pallets and plastic turnover boxes are two distinct unit-load tools: pallets (typically 600x800 to 1300x1150 mm footprint, 4-way fork entry) carry loose cartons, while pallet boxes / turnover boxes (202-1,400 L, HDPE walls, stackable) hold bulk or part loads. Selection hinges on payload weig
Selecting a capping and sealing machine in 2026 hinges on container format, throughput target, cap type and CIP/SIP requirements, with induction, spindle and chuck cappers covering most plant needs.
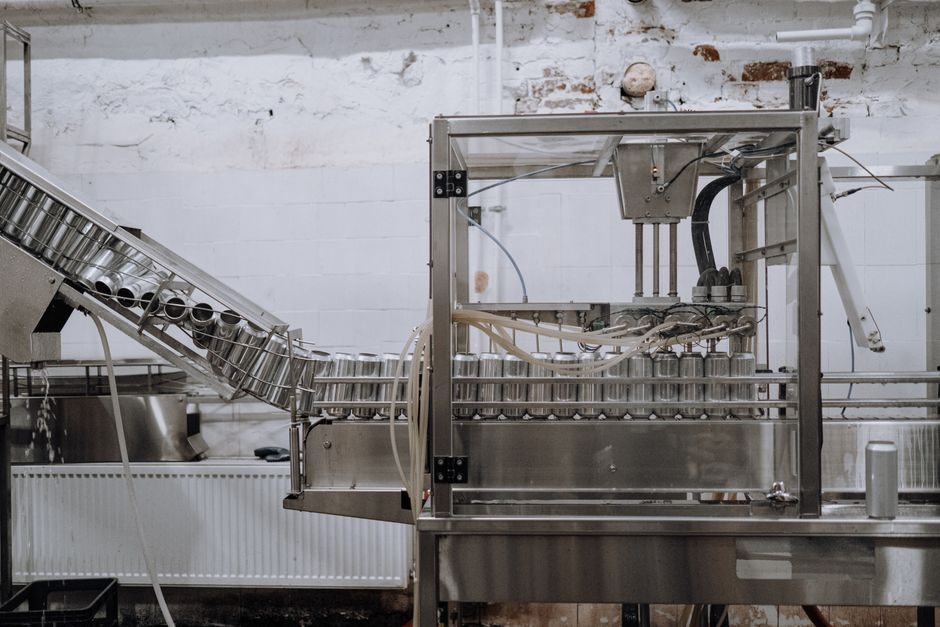
Chain conveyor selection hinges on seven hard gates: material density, pitch, drive load, environment, temperature, abrasion, and span. Rulmeca 138 PVC/steel 40-63 mm rollers suit light FMCG; FDN/FDR metal 76-89 mm rollers handle heavy unit accumulation.
Carton erecting machines form RSC/ HSC cases at 15-60 cpm before fill, while labeling machines apply front/back/wrap labels at 30-200 ppm on sealed packs — two complementary, non-substitutable assets. Selection hinges on throughput, box-format rigidity, and label-substrate chemistry rather than bran
Stretch film and strapping band serve different unit-load functions: stretch film uses elastic cling and pre-stretch to bind loose palletized goods, while strapping band uses tensile rigidity in PP or PET to lock rigid loads. Selection hinges on load rigidity, transit hazard, and equipment level.
Coding machine selection in 2026 hinges on substrate, throughput and ribbon chemistry. Continuous inkjet (CIJ), thermal transfer overprint (TTO) and laser dominate factory coding, with print speed, IP rating and message-change latency as the primary differentiators across pharmaceutical, food and wi
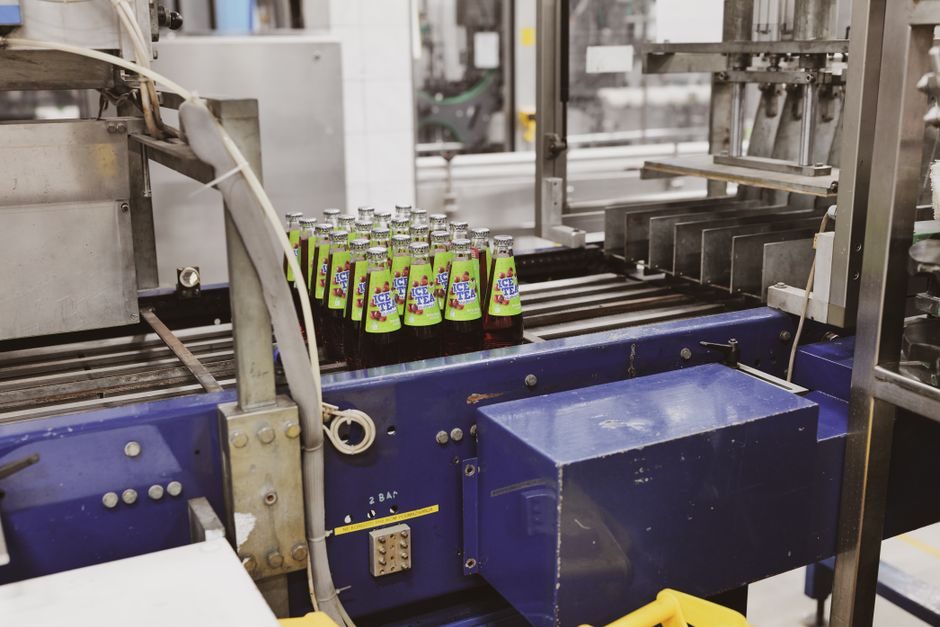
A shrink wrapping machine consolidates unit packs into a heat-shrunk film bundle, while a filling machine meters product into containers; the two are typically deployed in series on beverage lines, with shrink throughputs from 600 p/h to 32,000 bph and filling prices spanning US$2,300-38,000.
Labeling machines in 2026 span US$1,500-55,000 on Made-in-China.com; select by container geometry, throughput and label type rather than cheapest unit price.
Labeling machine selection in 2026 hinges on container format, label stock, throughput duty and control topology; match sleeve, adhesive or OPP hot-melt platforms against line speed, container OD and CIP exposure before comparing vendors.
Overhead conveyors span monorail, double-rail, power-and-free and rope-driven variants, with 2026 vendor catalogs listing 88+ products from 41 manufacturers, MOQ pricing on chain units from US$480-680/m, and dual-rail light-duty ratings around 100 kg load.
Bucket elevator selection is a four-gate engineering decision: capacity vs lift height, bulk density, material abrasiveness/abrasion class, and a centrifugal/positive/super-capacity continuous-discharge type match, all set before any chain, belt, or horsepower call.
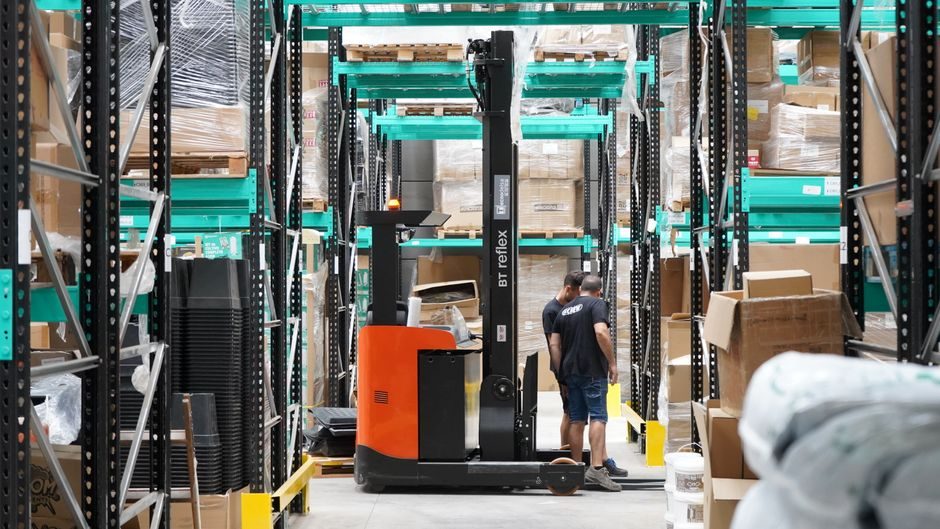
Electric pallet trucks and reach trucks split on lift height, aisle width, and load geometry: pallet jacks cap near floor level at 1,800–2,000 kg, while reach trucks extend forks 4–12 m at 1,000–2,500 kg. Match by SKU density, not price.
A checkweigher is an in-line QC device that dynamically weighs every pack on a conveyor to flag over/under-fill rejects; a filling-weighing scale is a static or semi-automatic dosing machine that dispenses product by weight. Pick the first for high-volume QA on sealed packs, the second for precise b
Hydraulic dock levelers dominate 2026 high-cycle warehouse specs, with vertical-storing models like Rite-Hite Genisys HL700 competing against air-powered Kelley aFX and mechanical / seal-hydraulic units; the right pick hinges on capacity, lip geometry, dock height range, drive type and duty cycle.
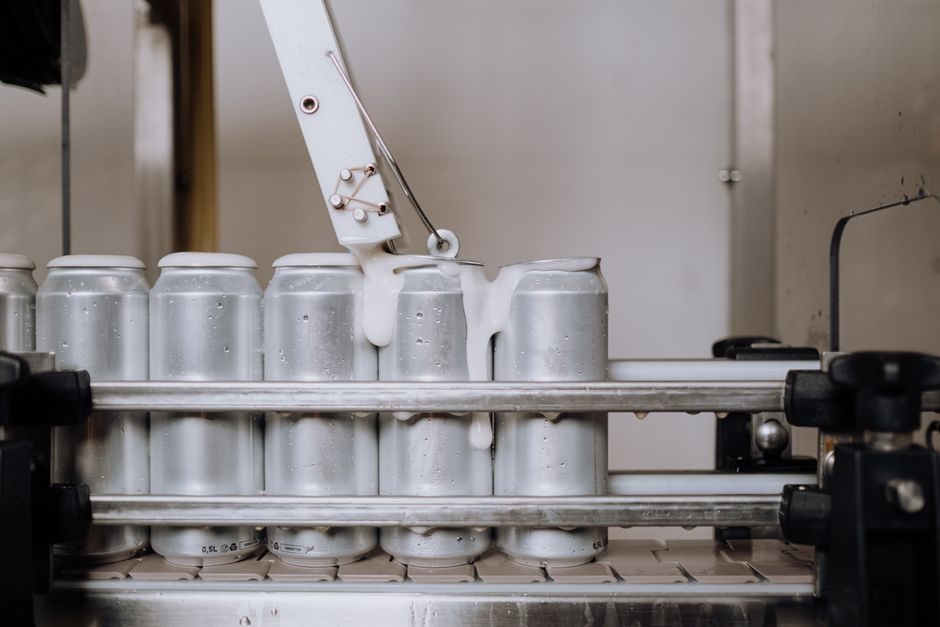
As of June 2026, Chinese-made automatic liquid filling lines for juice/beverage applications list at US$20,000-200,000 per set on Made-in-China.com, while automated rotary premade-pouch doypack liquid fillers run US$52,000-67,000 and pharma-grade lines from 25-year specialists sit above that ceiling
Strapping machines apply tensioned PP/PET strap with a heat-seal or metal clip to unitise cartons and pallets, hitting 30-65 cycles/min on automatic models. Shrink wrapping machines use LDPE/PO film and a heat tunnel to collate multi-pack loads, typically 30-60 packs/min. Pick by unit-load type: rig
Truck scales handle 30-100+ tonne legal-for-trade bulk loads at low speed, while checkweighers verify 0.05-50 kg packaged units at line speed; selecting the wrong class costs 2-10x in capital and accuracy.
Strapping machine buying guide 2026: semi-automatic, automatic, and fully-automatic units built around PP/PET/steel strap with cycle rates typically 20-65 straps/min, and 2025 market size USD 5,520.2 M growing to USD 8,155.2 M by 2033 at 5.1% CAGR per Grand View Research.
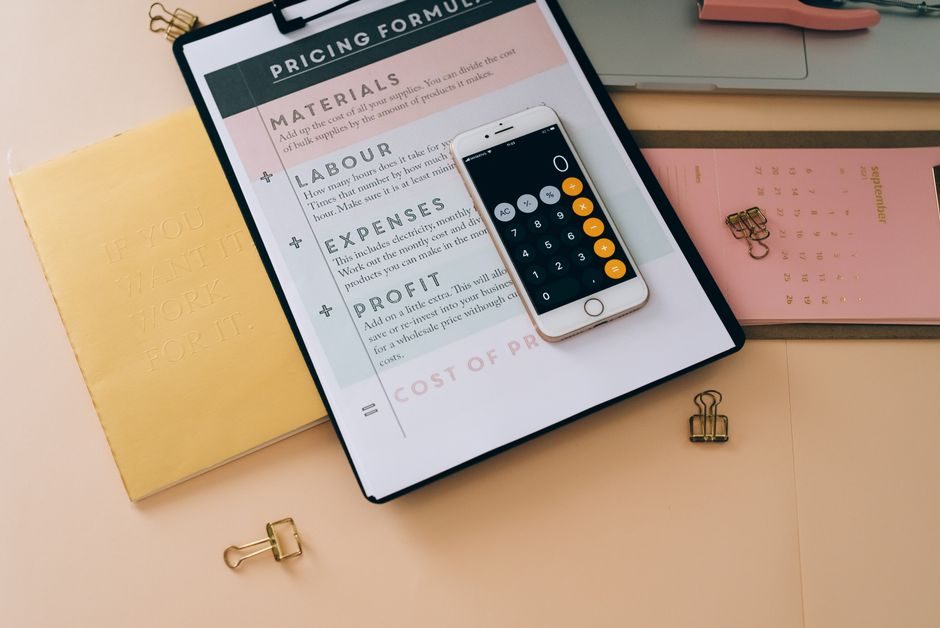
As of June 2026, a new 5,500 lb manual pallet jack lists in a $200–$900 spread on Alibaba, while US retail benches (Dayton, Lift-Rite) sit near $740 and a used 5,500 lb hand truck clears around $1,400; total cost of ownership is driven mainly by spec class, not sticker.
Reach trucks lift 1.0-2.5 t loads to 6-12 m in 2.5-3.0 m narrow aisles; platform trolleys move 150-500 kg manually on flat floors. Pick reach truck for palletized rack work, trolley for light, short-haul order picking.
Roller conveyor unit cost in 2026 spans roughly USD 30 for a single light-duty galvanized steel skate-wheel to USD 4,000 for a heavy-duty curve section rated 1,800 kg, with system price driven by roller diameter, frame material, load class, and driven-vs-gravity configuration.
New hydraulic dock levelers from Chinese OEM lines price at US$950-2,200 FOB per set in 2026, with European 6,000-9,000 kg hydraulic units typically 3-5x that band once installed in the EU.
Bucket elevators win on vertical lift and high-capacity dry bulk; screw conveyors win on horizontal/inclined enclosed transfer of fine or semi-fluid material. Pick by lift height, particle size, moisture, and whether the line runs inclined or straight-up.
Chain conveyor quotes in 2026 are driven by chain spec, throughput and layout, with horizontal redler units rated 38–230 t/h and POM slat chain at ~1,100 N tensile strength forming the typical low-to-mid cost band.
Hydraulic dock levelers dominate 2026 industrial-buyer RFQs, with vertical travel of 305-610 mm and dynamic capacities typically rated 45,000-80,000 lb per EN 1398 and OSHA 1910.30 loading-dock rules.
Turnover box selection in 2026 hinges on seven spec gates: load rating (typically 10-75 kg), material grade (PP/HDPE for plastic, SUS 304/201 for metal), volume (15-75 L common), stack/hinge lid design, food-grade certification, MOQ economics, and supplier audit. Hit all seven to avoid line-stoppage
Electric pallet trucks (EPTs) for 2026 fleets typically span 1.5–3.0 t capacity, 24V/48V lead-acid or Li-ion, AC drive, with ride-on and stand-on variants. Spec around battery chemistry, IP rating, service brake, controller and load-wheel spec — not sticker price.
Customized belt conveyors list at US$1,200–7,800 per piece on Made-in-China as of 2026-05, while cement-rated fixed systems run US$2,920–680,000 and nylon belting sits at US$1.40–20.00 per metre. Total installed cost is driven by belt type, idler/pulley spec, drive size and structural steel, not jus
Chamber vs belt vs vertical vacuum packers split 2026 sourcing by food, pharma or hardware duty; tabletop 400 mm class bell units dominate the sub-USD 3,000 entry band, while 28+ OEM lines on DirectIndustry confirm 16+ active manufacturers.
Screw conveyors (augers) move 0.5-500 TPH of bulk solids in trough, tubular, and vertical configurations. Selection hinges on material bulk density, abrasiveness, incline angle, and shaft vs. shaftless design. 142 manufacturers list 241 units on DirectIndustry.
2026 AMR buying decisions turn on three spec lines: payload (light <100 kg vs heavy 1,500–1,900 kg), navigation stack (LiDAR-SLAM vs magnetic/vision tape), and safety compliance to ANSI/ITSDF B56.5 and ISO 3691-4. Match fleet management and battery duty cycle to your throughput before vendor sele
Vertical lift module (VLM) price for 2026 typically runs USD 60,000–250,000 for the unit, with installed cost 1.4–2.2× the list price once trays, integration and site work are added; sizing, throughput and load class drive most of the swing.
Specifying a capping and sealing machine in 2026 comes down to four gates — cap format, throughput, torque/pressure accuracy, and IP/hygiene rating. Small semi-auto pneumatic crimpers quote from US$1,500; integrated pharmaceutical lines with vial filling and capping sit at US$9,150 per set MOQ-
Stacker cranes in 2026 follow ASME B30.18-2011 duty classification, pair variable-speed drives with PLCs per ABB and Mitsubishi Electric, and split into unit-load vs miniload configurations with mast heights above 40 m in modern AS/RS builds.
2026 order picker buying is dictated by lift height, platform capacity, aisle width and floor class; manual stock pickers suit sub-3 m pick faces below 250 kg, while electric rider units are the default once faces exceed 4 m or 1,000 kg/shift.
Manual pallet jack selection is governed by five engineering gates — load capacity, fork dimensions, lift height, wheel/roller material, and pump/tiller geometry — with 5,500 lb (2,495 kg) and 48×27 in forks defining the dominant US warehouse class.
Platform trolley buying in 2026 hinges on load class (150-500 kg), wheel material (TPR/PU/nylon/cast iron), deck gauge and MOQ. Verified S2 listings show US$10-32/pc FOB China at 100-piece MOQ, with Indian OEM offers near US$79 from Trust Traders.
PET strapping band selection turns on four hard gates — width × thickness (load rating), core material (PP / PET / steel), elongation class, and joint method (heat-weld, buckle, battery tool) — verified against strapping-machine cross-fit. PP suits light palletizing under 200 kg; PET covers 200–1500
Carton box sourcing in 2026 is decided by flute profile, ECT/BCT rating, board grade and FOB band — single-wall 3-ply moves 5-15 kg, double-wall 5-ply handles 15-40 kg, triple-wall crosses 60 kg+. Price spreads run from ~USD 0.15 to USD 1.80 per piece FOB China.
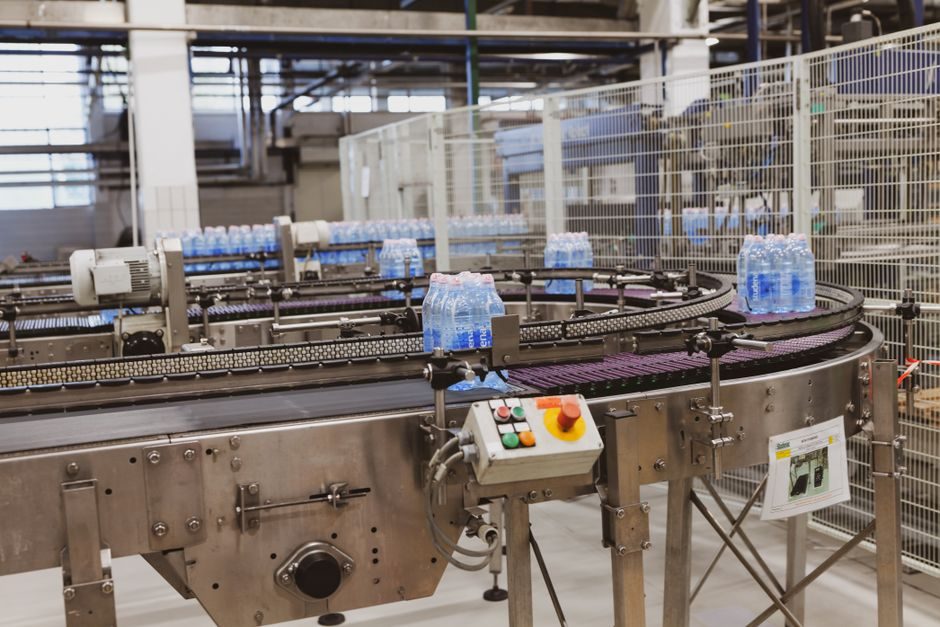
Screw conveyor selection is a five-gate decision: material class, capacity/length/incline, trough vs tubular shafted vs shaftless, drive HP, and abrasion/corrosion service. Get any of these wrong and the unit either plugs, overloads, or wears out in months.
Filling scales and bench scales share a load-cell core but diverge on throughput, accuracy and integration: filling scales meter product into containers at line speed, bench scales verify small-batch mass on the workstation. Spec the wrong one and you either overpay for capacity you do not need or s
Order pickers lift people and pallets to picking height; dock levelers bridge truck beds to warehouse floors. They serve different workflows — picking vs. loading — and should be compared by lift height, capacity, drive type, cycle, and footprint, not by "which is better."
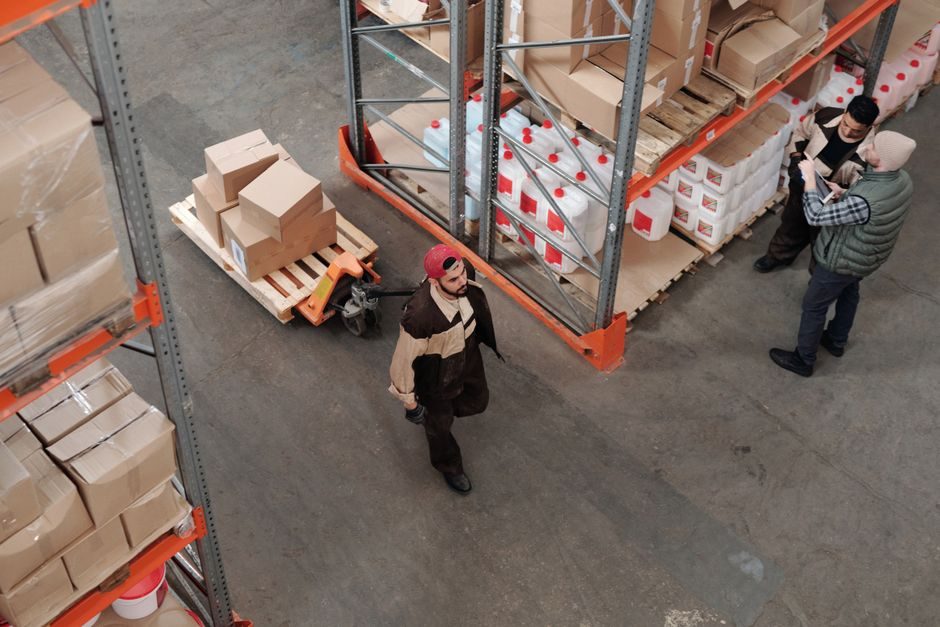
Electric pallet truck selection hinges on six gates: load class (1.5-2.5 t typical, 3.0 t heavy), drive configuration (walk-behind vs platform), battery voltage (24V/48V), fork dimensions, chassis height for the racking interface, and operator ergonomics under ISO 3691-1 / EN 1726 truck safety rules
New industrial strapping machines from Chinese OEMs sit in a US$800–8,500 FOB band on Made-in-China.com (June 2026), with full-automatic pallet units 2× the price of semi-automatic tabletop units. Steel, PET and PP strap compatibility, table-top vs pallet-portal form factor, and CE/ISO 9001 document
Dock levelers and manual pallet jacks solve two different bottlenecks at the loading bay: vertical drop and horizontal pallet move. A 6600 lb manual truck with 27x48 in forks pairs with a 25-35 ton rated hydraulic leveler for typical 4-6 trailer/hour docks.
2026 case packing machine selection hinges on throughput, pack pattern, integration interface and after-sales coverage; Chinese OEM case packers start around USD 12,300 per set FOB with 1-year warranty, while custom turnkey lines from US/EU integrators are quoted project-by-project within 1 business
Chain conveyors in 2026 are specified by load class, chain pitch, layout geometry and drive type; capacities range 8 kg per carrier to 1000 t/h bulk, with 190 mm effective width for spiral food/pharma lines.
New electric pallet trucks (EPTs) list between US$400 and US$5,500 ex-works in 2026, with 1.4–2.5 t walk-behind units clustering at US$469–2,000, lithium 48 V models at US$2,800–3,500, and ride-on platforms at US$4,500–5,500. Battery chemistry, capacity, drive class and MOQ are the four real quote l
AMR pricing in 2026 is driven by payload class, navigation stack, and battery chemistry, with entry units below $25K, mid-range fleets at $30K-$75K, and heavy-duty systems from $80K to $200K+ before integration.
New narrow-aisle reach trucks list from US$14,600 FOB China for a 2,500 kg battery stacker, while 2026 Raymond 7200 configurations target grade, cold-storage and aisle-density trade-offs; used Latvian units on Mascus give a 2026 used-fleet floor.
Roller conveyor selection in 2026 hinges on six gates: load class, drive type, roller diameter, frame profile, environment, and integration. DirectIndustry lists 225 manufacturers and 581 products for category roller conveyor, with pallet-rated electric modular lines spanning 1,500-4,500 kg per
AS/RS selection in 2026 hinges on seven engineering gates — throughput SKU profile, cube height, load unit, fire code, WCS interface, brownfield fit, lifecycle cost — that decide between unit-load, mini-load, shuttle and vertical-lift module architectures before any RFQ goes out.
Filling machines dose product into a container; carton erecting machines form the empty container itself. They sit on opposite ends of a packaging line, run at very different speeds, and are specified against different decision criteria, so they are never a like-for-like swap.
Vertical Lift Modules trade floor area for height at roughly US$1.77 B market by 2031, while pallet racks dominate low-SKU, high-throughput pallet flows on capital cost per bay. Pick by SKU profile, throughput, ceiling height, and amortised pick cost — not by brochures.
Vacuum packaging machine prices in 2026 span $1,300 to $61,000 across tabletop, chamber and thermoforming builds, with chamber size, pump capacity, body material and automation driving the 90%+ spread.
Vibrating conveyors move bulk solids and packaged goods on a trough or spiral track driven by an eccentric mass or linear motor, with 2026 OEM offerings spanning stainless 304 alignment shakers, spiral vertical lifts, and hybrid VIBRA-BELT trough-belts at throughputs from 5 to 20+ t/h
Bench scales cover 0.1 kg to ~600 kg on a 300–600 mm stainless or carbon platform, IP65–IP68, while truck scales handle 30–150 t on 6–24 m steel decks — the choice is capacity, footprint and accuracy class, not price.
Chain conveyors move unit loads up to 10,000 kg on powered tracks and accumulate them mid-line; vibrating conveyors shake bulk solids at 0.5–6 m/s on troughs. Pick by load type, not tradition.
Steel strapping (AISI 201/304/316) dominates heavy-duty load securement, while PP and PET strapping cover 60-80% of carton and pallet shipments; 2026 buyers should match band width, thickness, tensile rating, and joint style to load class before sourcing.
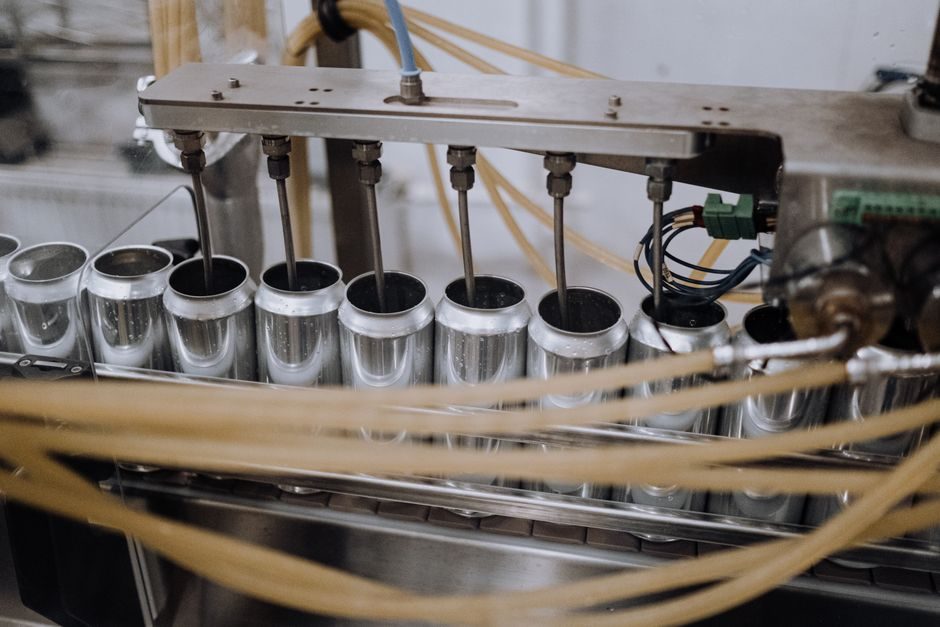
Overhead conveyors and roller conveyors solve different handling problems: overhead systems move work-in-progress above the floor on a powered chain or monorail, while roller conveyors shift cartons, totes and pallets along a floor-level gravity or driven line. Pick overhead for paint lines, garment
2026 truck scale buyers face four structural choices — pit vs above-ground, analog load cells vs digital POWERCELL PDX, axle-group certification vs full-deck, and steel deck vs concrete deck. Each lever swings 15-40% of installed cost, and the wrong call forces a costly retrofit on the next legal-me
China-made PP strapping band FOB bands sit at US$14.00-20.00 per roll (1-roll MOQ) while bulk-ton orders of 100+ tonnes run 800 t/week supply capacity from Sichuan plastic plants, reshaping 2026 landed-cost math.
Manual pallet jacks in 2026 span a 2,200-5,500 lb capacity range across light-duty and heavy-duty tiers, with Chinese OEM frames from US$80/sq ft and aftermarket wheel kits available for legacy units. Selection is driven by load class, fork dimensions, pump design, and steer-wheel material.
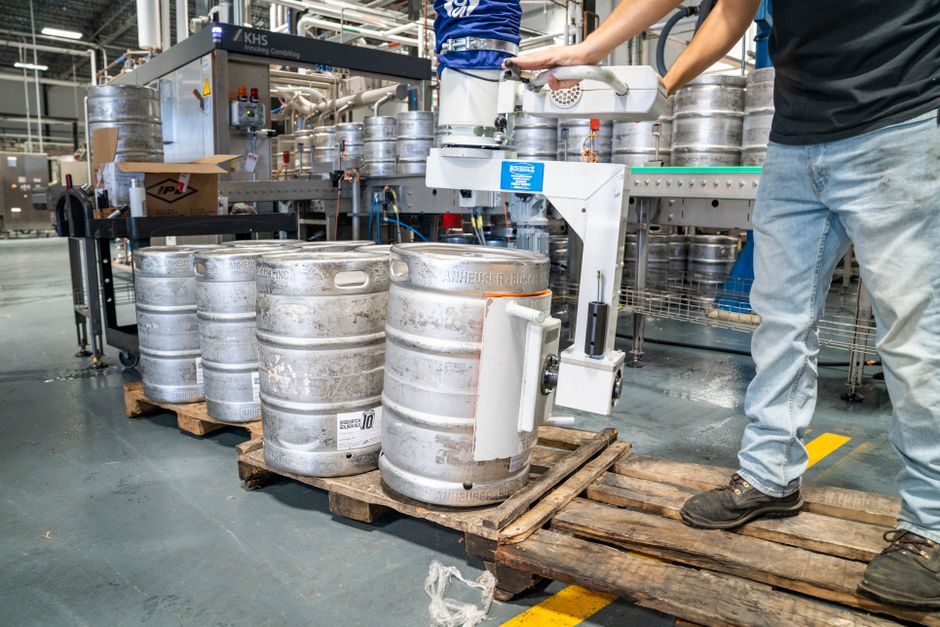
Pallet stackers 2026 split into semi-electric walkies (1.0–2.0 t, 1.6–3.5 m lift), rider pallet stacker trucks (1.3–2.0 t), and fully automatic stacker-destacker cells (15/25-pallet PALOMAT magazines) — selection pivots on load, lift height, aisle width and power source.
Specifying a filling scale in 2026 is dominated by four levers — head type (multi-head vs linear), weigh resolution 0.1–10 g, contact material (SS304/SS316L), and legal-for-trade OIML R76 approval — with Made-in-China listed units clustering around US$1,500–5,000 per piece.
Coding machines and vacuum packaging machines solve different plant-floor problems: ink/laser marking applies variable data to surfaces, while vacuum packaging extracts air from a sealed bag or chamber to extend shelf life. Spec them as two independent workcells, not alternatives, on any 2026 food,
Case packers and coding machines sit at different points on a packaging line: a case packer groups product into shipper cartons at 30-120 cpm, while a coding machine prints batch, date or variable data on individual units or cartons at 100-600 units/min. Use both together on FMCG/food/pharma lines,
Mesh belt conveyor selection in 2026 hinges on five engineering gates: belt material class (PTFE, SS304/SS316, polyester), continuous operating temperature window, product load per square metre, mesh opening size, and drive/speed envelope. PTFE mesh belts run -140 °C to +260 °C continuous, peaking a
Walk-behind electric pallet stackers start near US$990 FOB China for 1.0–1.5 t units; 1.4–2.0 t ride-on platform models (Linde L AP, TCM SP) occupy the US$5,000–12,000 band depending on mast height and battery. Plan total cost across machine, battery, charger, mast and service.
Mesh belt conveyor selection in 2026 hinges on matching belt weave, alloy grade and drive layout to temperature, load and product geometry. Buyers should lock thermal rating, mesh count and tension method before comparing suppliers.
New 2026 listings on ScaleTrader show used NTEP-certified truck scales priced from $33,000 for a 35 ft Mettler Toledo VTS100 to $150,000 for an 87 ft POWERCELL PDX off-road unit, while new full-length concrete-deck installs commonly run $50,000-$120,000 before load-cell, indicator and foundation wor
Conveyor sorting lines handle 2,000-10,000 items/hour on fixed-path rollers, belts, or cross-belt slats and dominate parcel and post-sort operations; shuttle systems (rack-mounted) excel where storage density and SKU variability drive ROI.
Filling scales in 2026 span roughly US$450 entry-level semi-auto units to US$25,000+ multi-head 10-head lines, with a typical 2-head 5–50 kg packaging scale landing US$1,800–4,500 FOB China. Real cost drivers are head count, weighing range, IP rating, material-contact grade and certification stack.
New electric order pickers list at roughly USD 18,000-45,000 in 2026 China export channels, while 2-3 tonne scissor-lift horizontal units from European OEMs run USD 28,000-55,000 FOB, with the total cost gap driven by lift height, battery chemistry and warehouse-aisle class.
Pneumatic conveying systems move dry bulk via air streams, with the global market projected to reach USD 48.36 billion by 2030. This 2026 buying guide covers dilute vs dense phase, component selection, and selection criteria.
A sorting system and an autonomous mobile robot (AMR) solve different problems: sorting systems identify, classify and divert mixed items at fixed stations, while AMRs transport payloads between waypoints on dynamic maps. Choose a sorting system for item-level recognition and throughput; choose an A
Capping/sealing machines apply torque, crimp or heat-seal a closure onto a filled container, while wrapping machines enclose a product in film or shrink sleeve; both sit on the same end-of-line conveyor but solve different package-integrity problems.
Chamber geometry, seal-bar length, ultimate vacuum and pump type drive 80% of a vacuum packaging machine spec. Buyers should match cycle time, bag size and product corrosiveness against chamber volume, kW rating and stainless grade before price.
Carton erecting machine selection hinges on throughput (up to 180 pieces/min), blank size range, PLC control architecture, and downstream compatibility with carton sealers and shrink wrap lines, per OEM data.
Screw conveyors suit horizontal-to-inclined dry bulk moves up to 45° with high solids-to-air ratios and low power per ton; pneumatic conveying systems handle longer runs, multiple discharge points, enclosed dust-tight transport for 0.5–150 t/h duties in 5–100 m pipelines.
Bench scale selection in 2026 hinges on capacity, readability, repeatability and connectivity fit. Industrial users typically match 0.01 g to 0.1 g readability to OIML R76 accuracy class, with rugged IP-rated housings for shop floor use.