A tire wheel balancer corrects a mounted wheel and tire assembly in service, while an industrial rotor balancing machine measures and corrects rotors for service speed, geometry, and production requirements [S1][S3][S6].
Choose by workload: wheel balancers serve passenger, light-truck, fleet, and heavy-duty assemblies, while industrial machines cover crankshafts, drive shafts, turbochargers, electric-motor armatures, fans, turbines, and other engineered rotors [S3][S5].
Separate Road-Wheel Service from Engineered-Rotor Control
A tire wheel balancer spins a complete wheel-and-tire assembly and determines the correction weight and angular location needed to balance it; technicians then add or remove rim weights [S7]. Its operating environment is an automotive or fleet workshop, and its correction target is ride vibration in a relatively narrow operating-speed band.
An industrial rotor balancing machine handles a defined rotating component with specified mass, diameter, width, speed, correction planes, and residual-unbalance limits [S6]. Automatic industrial machines can measure and correct without manual intervention and can be integrated into production lines [S5]. For wider guidance on the balancing principle, see static, couple and dynamic unbalance for rotors.
The practical distinction is not simply accuracy. A wheel balancer is optimized around rim geometry, adapters, clamp diameter, wheel mass, and road-wheel workflow. An industrial machine is optimized around rotor support, allowable residual unbalance, correction method, production integration, and operating speed.
Compare Capacity, Planes, Accuracy, and Correction
Portable wheel balancers can handle assemblies below 30 kg, offer measurement uncertainty down to 1 g, and complete standard measurement cycles in 4.7–7 seconds [S2]. Professional tire equipment is described as measuring imbalance to 1 g or less [S2]. These figures suit road-service decisions, not acceptance of an engineered rotor to a specified g·mm residual.
Industrial static balancing corrects in one plane and is appropriate when diameter is large relative to length, including discs, flywheels, fan wheels, brake rotors, and grinding wheels [S6]. Dynamic balancing corrects in two or more planes and is needed where mass distribution along the axis can create force and couple effects [S1][S6].
Select the Balancer for the Actual Workpiece
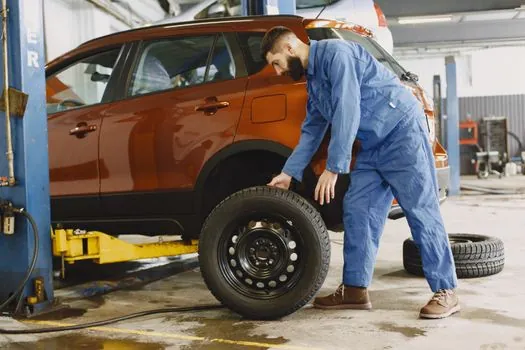
Select a wheel balancer when the required output is a road-ready wheel-and-tire assembly. Static wheel balancers serve low-volume or specialty work, while dynamic balancers remove static and couple imbalance and are the normal choice for modern tire shops [S3]. Heavy-duty versions are required for truck, bus, and commercial assemblies beyond the capacity of passenger equipment [S3].
Select an industrial balancing machine when the rotor has engineering-defined acceptance limits. The initial correction-plane choice should follow rotor geometry, residual static and couple limits, and operating conditions [S6]. Hard-bearing machines use rigid supports with little movement, while soft-bearing machines permit controlled movement of the rotor and are suited to different support requirements [S1].
Choose hard-bearing or soft-bearing construction around the rotor and test method, not around the terms “precision” or “industrial.” Choose a dynamic balancing machine when two-plane or multi-plane correction is justified by rotor geometry and operating speed.
Match Workflow, Volume, and Correction Method
For a tire shop, evaluate wheel diameter, width, offset, mass, vehicle class, and the most common assemblies before comparing cycle time. Automatic 3D balancers reduce manual measurement, use sensor-based rim acquisition, and may use pneumatic clamping and laser weight placement; cited equipment can complete a measurement cycle in 4.7–7 seconds [S2][S3].
For industrial production, the shop versus in-situ balancing guide provides a separate decision framework for whether the rotor should be balanced on a shop machine or at its installed operating position. Automatic balancing systems can handle measurement through correction and integrate with a production line [S5].
The correction method changes the workflow. Industrial technicians may add weights by welding, bolting, or pressing in slugs; remove material by drilling, milling, or grinding; or use laser machining where extreme precision is required [S1]. Wheel balancers instead add or subtract standardized weights at the rim [S7].
Protect Accuracy Through Setup and Verification
An industrial machine must therefore be selected around the rotor’s actual operating speed, permitted residual unbalance, support configuration, and correction planes, not simply by maximum rotor diameter.
Wheel balancing also depends on correct setup. Do not treat load-roller testing as a substitute for correcting the wheel’s mass imbalance.
Before acceptance, verify repeatability with the production fixture, adapter, shaft, and correction method that will be used. Industrial machines must meet the applicable ISO 21940 framework for balancing-machine evaluation and use, while the residual-unbalance target still depends on the rotor, speed, and application [S8]. For rotor-condition verification, an industrial borescope can support inspection of internal surfaces, but it does not measure residual unbalance.
Account for Limits, Failure Modes, and Service Requirements
Neither category solves every vibration problem. Static balance does not guarantee dynamic balance because opposite heavy locations can cancel when stationary while producing a rotating couple [S1]. A tire can also carry structural defects that a mass-unbalance balancer cannot correct, including ply distortion and stiffness variation detected through diagnostic load rollers [S2].
Unbalance produces speed-related vibration, noise, friction, and accelerated wear of bearings, seals, and shafts [S1]. An imbalance up to 50% more destructive to bearings than other vibration sources at equal vibration level is described in the cited reference, but that value must not be substituted for a machine specification or an ISO 21940 residual limit [S1].
For a tire shop, floor space, technician training, spare adapters, service support, and shop-system integration can outweigh a small difference in cycle time [S3]. For industrial equipment, bearing capacity, allowable speed, rotor mass limits, correction-plane control, residual-unbalance repeatability, and automatic line integration are more relevant than automotive workflow features.
A wheel balancer is the correct tool for a mounted road wheel and its tire defects; an industrial balancing machine is the correct tool for an engineered rotor with defined geometry, speed, and residual-unbalance requirements. Record the workpiece range, operating speed, correction planes, residual target, accuracy class, and correction method before comparing quotations.