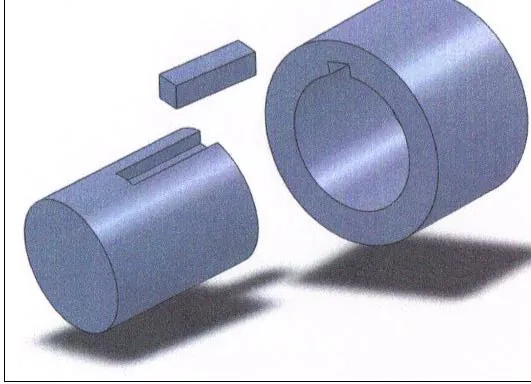
A shaft key is a small machined bar of metal that sits in a slot cut across the shaft and the bore of a mating hub, transmitting torque between the two by shear and bearing on its side faces. It is the simplest and most widely used demountable connection in power transmission, found wherever a gear, pulley, sprocket, coupling, or flywheel must turn with a shaft yet still be removed for service.
Start shaft key selection with the shaft and hub drawing. Establish the dimensional standard and edition, metric or inch units, key form, keyway dimensions and fit before checking torque, effective length and material. Dimensional conformity is not a load-capacity approval, and an ordinary key must not be assumed to provide calibrated overload protection. [S1]
This six-chapter reference separates key geometry from fit and load capacity. The size tables are working extracts, not automatic conversions between standards. ISO/R 773 is a historical reference; use the specified drawing and edition for an existing machine. Seven FAQs cover selection, effective length, materials and compatibility. [S1][S2]
Chapter 1 / 06
What is a Shaft Key
A shaft key is a machine element, usually a rectangular or square bar of steel, fitted into matching slots called keyways or keyseats that are cut into a shaft and into the bore of the component mounted on it. When torque is applied, the key transmits the rotational load between shaft and hub through shear across the key and bearing pressure on its side faces. Keys are one of the four classical methods of fixing a hub to a shaft, alongside splines, interference (shrink) fits, and friction-based locking assemblies, and they remain the most common because they are cheap, standardized, and easy to assemble and dismantle.
A key positively couples shaft and hub to transmit torque through its loaded faces. Its material, fit and effective engagement must be checked together with the shaft and hub. A replaceable key is not automatically a mechanical fuse: predictable overload protection requires an expressly designed and verified protective arrangement. ASME B17.1 defines dimensional relationships but excludes key strength and steel analysis from its scope. [S1]
The geometry has three named features that appear on every drawing. The keyway in the shaft is the longitudinal slot milled along the shaft surface; the keyway in the hub is the matching slot broached through the bore; and the key itself bridges the two. For a parallel key the sum of the shaft keyway depth and the hub keyway depth equals the key height plus a small clearance specified by the standard, so the key seats fully without bottoming or floating. Corner radii at the bottom of the keyway are specified deliberately, because a sharp internal corner is a fatigue stress raiser and is a frequent origin of shaft cracking.
Keyed joints have a long industrial history, and older machines may retain drawings written to superseded or withdrawn specifications. Parallel, taper and gib-head keys should be identified by the actual machine drawing and ordered standard, not by a claim that one historical recommendation governs every current joint. In particular, ISO/R 773:1969 is a historical reference identified by AGMA as withdrawn in 1998. ASME B17.1 has a separate dimensional scope. Preserve the specified edition and verify the key, shaft and hub details before approving a replacement. [S1][S2]
In scale terms, keyed connections span an enormous range. The smallest standard metric parallel keys are 2 mm wide and serve shafts of 6 to 8 mm in instrument drives and small gear motors, while the largest tabulated sizes exceed 100 mm in width on rolling-mill spindles and large marine reduction gears carrying shafts of several hundred millimeters. Across that range the underlying physics is identical: torque becomes a tangential force at the shaft surface, and the key must carry that force in shear and bearing without failing or working loose, which is exactly the calculation a procurement or design engineer must be able to check.
Chapter 2 / 06
Key Types and Classification
Keys are classified first by whether they are sunk into the shaft or not, and second by their cross-sectional shape and how they transmit and locate load. The great majority of industrial keys are sunk keys, meaning the keyway is cut into the shaft so the key sits partly below the shaft surface. Within that family the parallel key dominates, but several other forms remain important for specific duties. The table below summarizes the main types, how each transmits load, and where each is typically used.
Key type
Cross-section
How it transmits load
Typical applications
Parallel (square)
Uniform, width = height
Shear and bearing on side faces, no preload
Shafts up to about 165 mm (6-1/2 in), general drives
Parallel (rectangular)
Uniform, width > height
Shear and bearing on side faces, no preload
Larger shafts, where a full square would weaken the shaft
Feather key
Parallel, clearance in hub
Side faces, hub free to slide axially
Sliding gears, shift forks, adjustable hubs
Taper key
Sloped top, taper 1:100
Side faces plus friction from wedging
Legacy and heavy machinery, no separate axial lock
Gib-head key
Taper key with a head
Same as taper key, head aids removal
Where a key must be driven out from one accessible end
Woodruff key
Semicircular segment
Self-aligning, side faces of the protruding top
Tapered motor shafts, small engine crankshafts, spindles
Parallel keys have a constant rectangular cross-section along their length and transmit torque only through their side faces, exerting no radial force on the hub. This is their great advantage: the hub stays concentric with the shaft, which matters for high-speed and precision drives where any induced eccentricity would cause vibration. Square parallel keys (width equal to height) are preferred on smaller shafts, while rectangular keys (width greater than height) are used on larger shafts so the keyway does not cut too deep and weaken the shaft. Because parallel keys provide no axial location, the hub must be held by a separate set screw, retaining ring, shaft collar, or shoulder.
Feather keys are a variant of the parallel key with a deliberate clearance fit in the hub keyway so the hub can slide axially along the shaft while still being driven in rotation. They are essential in sliding-gear gearboxes, shift mechanisms, and any application where a component must move along the shaft under load. A feather key is often fastened to the shaft with one or two screws so it travels with the shaft rather than the hub, and it always uses the free-fit width tolerance described in Chapter 5.
Taper keys and gib-head keys have a sloped top face, conventionally tapered at 1:100, and are driven axially into the keyway so the wedging action grips the hub by friction in addition to the side-face contact. This lets a taper key hold a hub axially without any other retaining device, which is why it survived in older and heavy machinery. The penalties are that the wedge can push the hub slightly off-center, raising eccentricity, and that removal can be difficult. A gib-head key adds a projecting head so a puller or drift can extract it from one end. The exposed head must be guarded because it is a clothing-snag and injury hazard on rotating machinery.
Woodruff keys are flat semicircular segments that seat in a deep half-moon pocket milled into the shaft, with only the flat top protruding into the hub keyway. The curved base lets the key rock to align itself, so it is self-aligning and tolerates the tapered shafts found on electric-motor stub shafts, small internal-combustion engines, and machine-tool spindles. Their dimensions are standardized in ISO 3912 and DIN 6888. The trade-off is that the deep pocket removes a large bite of shaft cross-section, so Woodruff keys are confined to light and medium torque on smaller shafts and are rare in heavy industrial drives.
Chapter 3 / 06
Dimensional Standards and Sizes
ANSI/ASME B17.1 and ISO/R 773 are not a metric-to-inch substitution table. ASME B17.1 covers key and keyseat dimensions, types and tolerances for single-key applications; it does not select shaft size or establish key strength. ISO/R 773:1969 is a historical metric recommendation, identified by AGMA as withdrawn in 1998. For DIN 6885, GB/T 1096, JIS B 1301 or an older machine drawing, verify the specified edition, key form, groove depths and tolerances rather than assuming identical content from the standard names. [S1][S2]
The following is a limited extract of Ganter's published DIN 6885 parallel-key cross-sections and associated shaft-diameter bands. It is not a complete machining or acceptance drawing. The first row includes both 6 mm and 8 mm; the other selected bands are over their lower bound and up to and including the upper bound. Keyway depths, depth-reference symbols and their tolerances are deliberately not reproduced here: obtain them from the applicable drawing or exact keyway standard. Matching b × h alone does not establish complete replacement compatibility. [S3][S4]
Shaft diameter band (mm)
Published key b × h (mm)
6 to 8, both endpoints inclusive
2 × 2
Over 10 to 12 inclusive upper bound
4 × 4
Over 17 to 22 inclusive upper bound
6 × 6
Over 22 to 30 inclusive upper bound
8 × 7
Over 38 to 44 inclusive upper bound
12 × 8
For an inch-dimensioned key or keyseat, use the actual ordered ASME B17.1 edition and machine drawing. ASME's public scope identifies the covered dimensions, types and tolerances, but is not a public numerical keyseat table. This page therefore does not reproduce an unverified inch-size or depth extract. Do not obtain an inch replacement by rounding a metric b × h value or applying an approximate shaft-diameter fraction. The following checklist identifies the records needed for a replacement decision, without inventing a numerical crosswalk. [S1]
Record to obtain
What it must identify
What it does not establish
Drawing and standard edition
Metric or inch system; key type and end form; required edition
Another standard is not interchangeable merely because its title mentions keys.
Key and shaft dimensions
Actual b × h × l; shaft band; keyway dimensions with their depth reference
Nominal stock size alone does not approve the machined joint.
Shaft and hub tolerances
Separate key-width, shaft-keyway and hub-keyway limits
A DIN tolerance label is not an automatic ANSI fit-class conversion.
Application and design approval
Material, effective engagement and approved load basis
A dimensional match does not prove torque capacity or overload protection.
After confirming the cross-section and key form against the drawing, select a standard length that fits the hub and provides the required effective engagement. Rounded ends, chamfers and interrupted contact can make effective bearing length shorter than nominal stock length. Confirm the available keyway and hub engagement before cutting key stock; the final length also needs the separate strength check in Chapter 5.
Chapter 4 / 06
Materials and Key Stock
Keys are made from key stock, which is precision-rolled or cold-drawn bar held to the width and height tolerances the dimensional standards require, so it can be cut to length and dropped straight into a standard keyway. The default material is medium-carbon steel, most commonly C45, which is the same alloy known as 1045 in the AISI system and S45C in the Japanese system. C45 in the normalized condition gives a tensile strength of roughly 570 to 700 MPa and a Brinell hardness around 170 to 210 HB; supplied cold-drawn, strain hardening raises the tensile strength to roughly 600 to 800 MPa while reducing ductility. This combination of strength, toughness, and low cost makes C45 the workhorse of general key stock.
Specify material and condition, not an intended weak link. Request the key-stock grade, heat-treatment or delivery condition, dimensions and traceability required by the machine specification. A material certificate, when required, supports that identity; it does not by itself establish the joint's torque capacity. Compare allowable stresses for the actual key, shaft and hub with the engineer's approved design basis. Do not deliberately weaken a replacement key or upgrade it to a stronger alloy without reassessing the joint. [S1]
Beyond plain carbon steel, several material grades serve specific duties. The table below summarizes common key materials and where each is appropriate.
Material
Approx. tensile strength
Why chosen
Typical use
C45 / 1045 / S45C carbon steel
570 to 800 MPa
Strength, toughness, low cost
General-purpose key stock, the default
Stainless 304
about 515 MPa
Corrosion resistance, hygienic finish
Food, pharma, marine, washdown
Stainless 316
about 515 MPa
Chloride and acid resistance
Chemical and coastal environments
Brass
about 340 to 470 MPa
Non-magnetic, non-sparking, light duty
Instruments, electrical, low torque
4140 alloy / induction-hardened
over 900 MPa
High strength and fatigue under shock
Heavy reversing and impact drives
Stainless steels 304 and 316 are specified where corrosion or hygiene rules out carbon steel. Both have lower tensile strength than C45, around 515 MPa, so a stainless key may need to be longer to carry the same torque, and the designer must re-check the shear and bearing margins rather than assuming a drop-in swap. Grade 316, with its added molybdenum, is preferred for chloride-bearing and acidic environments such as coastal, marine, and certain chemical-process drives, while 304 covers general corrosion and food contact.
Brass keys are used where a non-magnetic or non-sparking element is needed, for example in instrument drives, certain electrical machines, and explosive atmospheres, accepting their lower strength for light-torque service. At the other extreme, alloy steels such as 4140, often induction or through-hardened, are chosen for heavy, reversing, or impact-loaded drives where a plain carbon key would peen or shear prematurely. In all cases the key material must be considered together with the keyway corner radius, surface finish, and fit, because fatigue cracking in a keyed joint usually starts at a sharp keyway corner rather than in the bulk of the key itself.
Chapter 5 / 06
Fits, Tolerances and Sizing
Once the cross-section is fixed by the shaft diameter, two engineering decisions remain: how tightly the key fits the keyways, and how long the key must be to carry the torque. Both are decided on the key width, because width controls the fit and width times length controls the shear area. Getting the fit wrong is the leading cause of keys working loose in service; getting the length wrong is the leading cause of keys shearing.
Metric keyway tolerance designations and ASME fit classes belong to their respective dimensional systems. Ganter's DIN 6885 key sheet lists key-width tolerance h9. Its separate DIN 6885-1 keyway extract shows the limited fit combinations below. They are not an ANSI class crosswalk or a universal application recommendation. State the key, shaft-keyway and hub-keyway tolerances separately, and verify the actual limits against the ordered edition and drawing. [S1][S3][S4]
Fit wording in Ganter extract
Shaft keyway width
Hub keyway width
Sliding
H9
D10
Loose fit
N9
JS9
Tight fit
P9
P9
A sliding, loose or tight seating must be selected for the actual joint, not inferred solely from a generic duty label. Ganter's extract also states that exceptions to its typical slot-width designation appear on the relevant standard sheet. Check the key's actual width limits and the shaft and hub limits together before machining or approving a replacement. A named fit combination does not establish torque capacity or convert a DIN tolerance into an ANSI fit class. [S1][S4]
Sizing the length starts by turning torque into a tangential force at the shaft surface. With T the transmitted torque and D the shaft diameter, the force on the key is F = T / (D/2) = 2T/D. The key then carries this force in two distinct ways, and both must be checked.
Shear stress acts across the width times the effective length: shear stress = F / (b × L), where b is the key width and L is the effective length. The key must not exceed the allowable shear strength of the key material.
Bearing (crushing) stress acts on the portion of the key height that presses against the keyway wall, approximately half the height: bearing stress = F / ((h/2) × L), where h is the key height. The key must not exceed the allowable compressive strength of the material or of the weaker of the shaft and hub.
For the simplified half-height bearing model above, a square key gives a calculated bearing stress twice its calculated shear stress. That geometric relationship does not establish which failure mode governs: the allowable stresses and effective contact depend on the key, shaft and hub materials and the design basis. Obtain those values from the responsible engineer rather than treating a generic C45 tensile figure as an allowable shear or bearing stress. ASME B17.1 itself does not supply a strength approval. [S1]
Apply the approved design torque, load spectrum and service factors consistently, check both shear and bearing against the permitted stresses, and choose a standard length that fits the hub. If engagement is insufficient, the designer must reassess the joint or connection type. Do not assume two keys share load equally or assign a universal percentage derating: ASME B17.1's stated dimensional scope is for single-key applications. [S1]
Chapter 6 / 06
Selection Decision Factors
To turn the preceding chapters into a specific part number, work through the decision sequence below. Most key failures trace not to a single wrong number but to skipping one of these checks, especially fit class and axial retention, which are the two most commonly neglected. This list doubles as an RFQ template.
Drawing and dimensions: confirm standard, edition, units, shaft diameter, key b × h, end form, groove depths and dimensional limits. Treat ISO/R 773 as a historical reference rather than a current universal substitute. [S1][S2]
Torque and engagement: use the approved torque and service factors, check effective length for shear and bearing, and confirm that the usable hub and keyway lengths support that engagement. Dimensional conformity alone is not a capacity check. [S1]
Key type: choose parallel for general fixed hubs, feather for axially sliding hubs, taper or gib-head only for legacy or heavy machinery that relies on the wedge for axial hold, and Woodruff for tapered or self-aligning small shafts.
Fit: specify the key-width and both groove tolerances under the chosen standard; do not convert metric fit descriptions into ANSI class numbers by name alone. [S1][S3]
Material and records: order the required grade and condition, with certification or batch traceability where the machine specification requires it. Reassess any changed key, shaft or hub material; do not assume a replacement key is a calibrated sacrificial element. [S1]
Axial retention: a parallel key gives no axial location, so specify the locking method separately, a set screw over the key, a retaining ring, a shaft collar, a shoulder, or a locking assembly. Omitting this is a frequent oversight.
Keyway detail: specify corner radii and surface finish at the bottom of the keyway to limit fatigue stress concentration, and confirm the broach and cutter sizes are standard so the joint is serviceable in the field.
Serviceability depends on retaining the drawing, exact key size and form, fit, material condition and supplier records. Keep replacements to that specification rather than substituting whichever stock appears close in size. A sheared or deformed key also calls for inspection of the hub and shaft keyways and investigation of the failure, not simply installation of another deliberately weaker key.
FAQ
What is the difference between a parallel key and a taper key?
A parallel key has a uniform rectangular or square cross-section along its length, whereas a taper key uses a wedging form. Identify the actual key type, end form and retaining arrangement from the machine drawing before ordering a replacement; neither its appearance nor a historical standard name establishes compatibility. ISO/R 773:1969 is a withdrawn historical reference, not a reason to assume that all modern parallel keys share one current specification. Keep key dimensions, keyway tolerances and load approval separate. [S1][S2]
How do I select the right key size for a given shaft diameter?
Identify the machine drawing, dimensional standard and edition, units, shaft-size band, key form and groove dimensions first. Then check fit, available hub engagement, material condition and the separate load calculation. Do not round between inch and metric stock or treat a nominal size match as complete interchangeability. ISO/R 773 is a historical metric reference, while ASME B17.1 covers its own dimensional relationships. [S1][S2][S3]
How is key length calculated from torque?
Using consistent units, the simplified tangential force is F = 2T/D. Check shear over b × effective length and bearing over the actual engaged height × effective length; the half-height expression in this guide is a simplified model. Apply the approved load factors and material allowables, not universal numerical allowances. The chosen nominal length must fit the hub and deliver the required effective engagement. ASME B17.1 does not establish key strength. [S1]
What material are shaft keys made from?
Key stock is available in carbon steel, stainless steel and other specified materials, but the grade and delivery condition must match the drawing and design basis. Request a material certificate or batch record when the purchase specification calls for one. A material name or certificate alone does not approve torque capacity, and an ordinary key should not be treated as a calibrated overload fuse. [S1]
What are the fit classes for keys and keyways?
Specify the key-width tolerance and the shaft and hub groove tolerances under the same stated dimensional system. Sliding, normal and close metric descriptions are not an automatic crosswalk to ASME class numbers. Verify limits and the required assembly behavior from the applicable standard edition and drawing; a supplier's DIN 6885 sheet, for example, identifies h9 key width separately from groove details. [S1][S3]
When should I use a Woodruff key instead of a parallel key?
A Woodruff key is a semicircular segment that seats in a deep half-moon pocket milled in the shaft, with the flat top engaging the hub keyway. It is self-aligning and tilts to follow a tapered shaft, which is why it is standard on tapered motor shafts, small engine crankshafts, and machine-tool spindles. Its dimensions follow ISO 3912 and DIN 6888. The drawback is that the deep pocket removes more shaft material than a parallel keyway and weakens the shaft, so Woodruff keys are limited to light and medium torque on smaller shafts and are uncommon in heavy industrial drives, where parallel keys are preferred.
Are ANSI B17.1, ISO/R 773 and DIN 6885 keys interchangeable?
Not automatically. Nominal metric sizes may correspond, but the key form, groove depths, dimensional limits, shaft-size band and standard edition must be checked before replacement. Inch ASME B17.1 dimensions are not obtained by rounding a metric key. ISO/R 773:1969 is a historical recommendation identified by AGMA as withdrawn in 1998; retain it where a legacy drawing calls for it, with the drawing's actual requirements. [S1][S2]