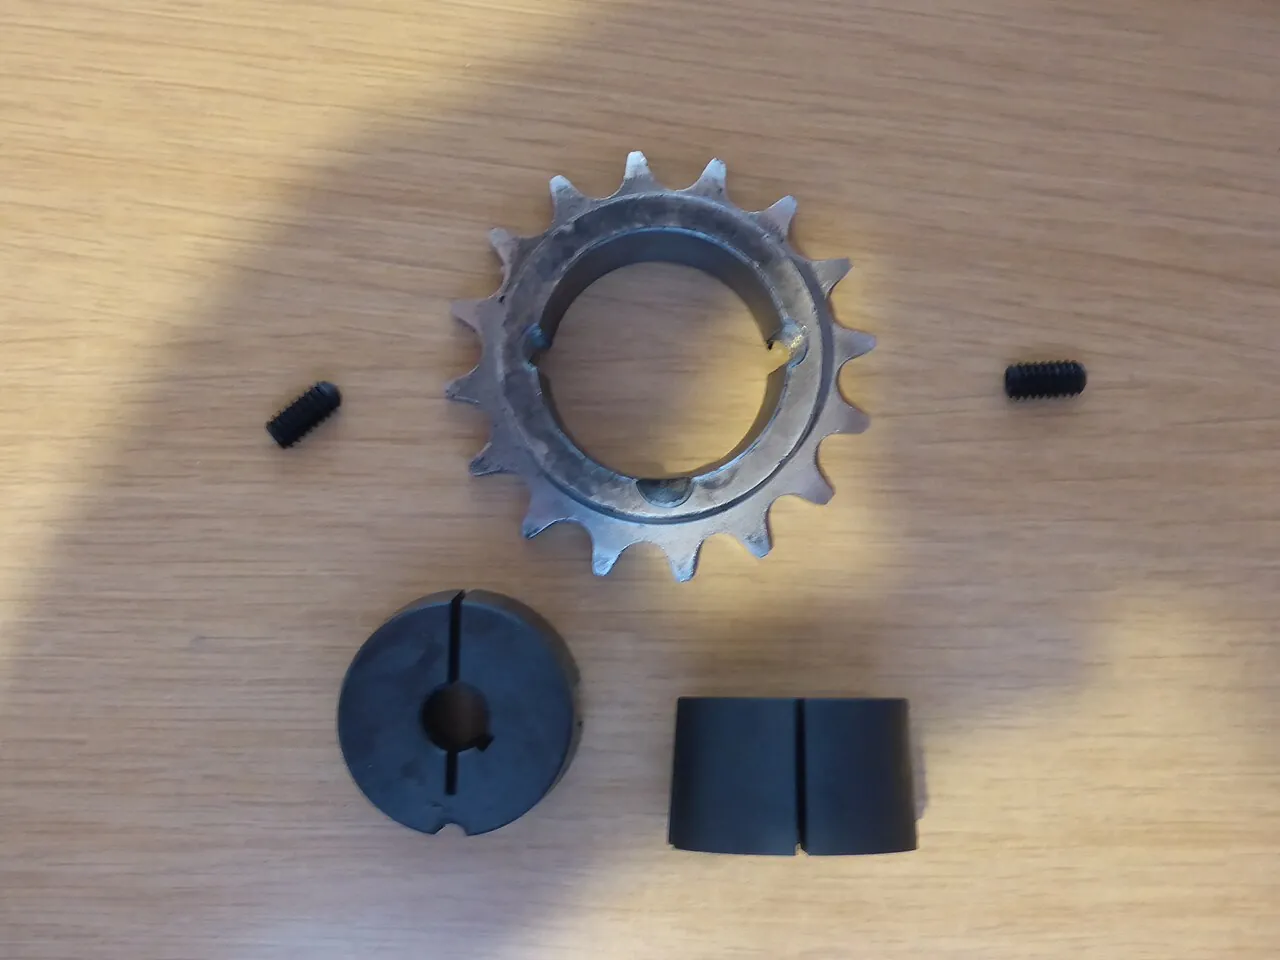
A taper bush is a split, tapered sleeve used to mount a pulley, sprocket, sheave or coupling hub on a shaft. The selected bush connects the component's tapered seat to a specified finished bore and keyway. Different shaft-fixing systems can look similar, so identify the actual manufacturer, family and series before ordering or planning maintenance.
Tightening holes and jacking holes do different jobs. Installation screws draw the bush and hub together; removal screws act at the maker's designated extraction positions to release the taper. The Martin drawing uses different symbols for these positions and states that each completed hole is threaded on one side only. Do not assume an empty hole is a spare tightening hole or identify the removal hole from generic prose alone. [S2]
This six-chapter guide covers bush families, clamping, material choices and replacement checks, with seven FAQs. Start with the maker's system drawing, finished bore, keyway and fastener specification. BS 4235-2 concerns Woodruff keys and keyways, not a general taper-bush interchangeability standard. [S1]
Chapter 1 / 06
What is a Taper Bush
A taper bush is a precision adapter between a cylindrical shaft and a matching tapered hub seat. Its split wall permits contraction as the prescribed screws bring the bush and hub together. The bore, taper geometry, screw arrangement and keyway belong to the selected system drawing. A part that looks similar or carries a familiar size code is not, by appearance alone, a confirmed replacement. [S2]
The fixing exists to solve a stocking and standardisation problem. Without it, a manufacturer of V-belt pulleys would need to machine and warehouse every pulley in dozens of finished bores: 19 mm, 24 mm, 28 mm, 38 mm, and so on, each with its own keyway. With a taper bush, the pulley is produced once with a standard tapered seat, and the bore is set by which bush is fitted. A single 2517 taper-bored pulley can be matched to any shaft from roughly 15 mm to 60 mm simply by ordering the correct bush. This decoupling of component from shaft is the central engineering value, and it is why the system has dominated industrial belt and chain drives since the 1950s.
Series codes make spare-part identification convenient, but they are not proof of universal interchangeability. Record the bush maker, family and series together with the mating component. BS 4235-2 is a Woodruff-key and keyway specification; it cannot substantiate a claim that all taper bushes bearing a size number interchange. Confirm the replacement against the actual component and bush drawings. [S1]
Functionally the taper bush competes with three other shaft fixings: the plain key-and-keyway with set screw, the keyless locking assembly (a frictional shrink-disc device), and the integral hub with set screws. Relative to a bare keyway it adds concentric self-centring and easy removal; relative to a keyless locking assembly it is far cheaper and lighter but transmits less torque and still relies on a key. Understanding where it sits on this spectrum is the first step in selection, covered fully in Chapter 6.
Four practical attributes determine whether a taper bush is right for a job: the available bore range for the chosen series, the rated transmissible torque and axial holding force, the material grade against the duty environment, and the ease of removal for maintenance. These attributes are decided at the series level, so picking the series correctly is the most consequential early decision. The remainder of this guide unpacks each in turn.
Chapter 2 / 06
Types and Series
Tapered shaft bushes divide into two broad families that look similar but are not interchangeable: the Taper-Lock bush, dominant in Europe and Asia, and the QD bushing, dominant in North America. A third group, the keyless tapered bush, dispenses with the keyway and relies purely on friction. The table below compares the families on the attributes that matter at selection.
For a Taper-Lock-type installation, distinguish the screw positions on the specific drawing rather than treating all apparent holes alike. Martin's instructions mark installation and removal positions differently, and require each completed hole to have threads on one side only. The familiar 1008, 1610, 2517 or 3030 code still needs a finished-bore and keyway specification. Use the supplied screws and the maker's matching component data. [S2]
The QD bushing achieves the same friction clamp but bolts axially against a flat hub face through the flange, which makes it quick to fit and strip without disturbing the taper seat. Its series are lettered rather than numbered: JA, SH, SDS, SD, SK, SF, E, and F in ascending size and torque capacity. Because QD installs dry and is bolted from the flange face, it is favoured where components are swapped often, such as adjustable conveyor drives. Importantly, QD and Taper-Lock are not cross-compatible: a hub bored for one will not accept the other.
The keyless taper bush family removes the keyway and grips the shaft entirely by friction generated by the taper clamp. This eliminates the backlash inherent in any key-and-keyway fit and avoids fretting under reversing or servo duty, at the cost of lower steady torque for a given size and tighter shaft tolerance requirements. It overlaps with the locking-assembly category. Finally, the Browning H, P, and Q bushings are a proprietary flanged taper system common in North American original equipment, dimensionally distinct from both Taper-Lock and QD, and generally only interchangeable within the Browning range.
Within the Taper-Lock series, every size is offered with metric bores, inch bores, and keyless variants, plus a choice of keyway standard. The same physical bush therefore appears in a catalogue many times, distinguished only by the finished bore and keyway. Always quote both the series code and the finished bore, for example "2517 bush, 42 mm bore, DIN 6885 keyway," to order unambiguously.
Chapter 3 / 06
The Taper Principle and Clamping
The holding action comes from the matching tapered bush and hub seat. Axial screw loading produces radial clamping as the split bush contracts onto the shaft. This explains why the correct hole position and fastener matter, but it does not establish a universal taper angle or a cross-brand fit. Read the actual manufacturer's drawing when checking geometry or replacing a component. [S2]
Clamping and release are different screw functions. The specified installation positions create the assembled grip; designated removal positions release that grip. Correct seating and retention also depend on the selected parts, surface condition and screw specification. Do not infer that vibration, supplementary locking or maintenance requirements are settled merely by a generic taper ratio. Follow the applicable maker's instructions. [S2]
The screw tightening torque is an installation value, not the drive's transmitted torque rating. The table below is a limited extract from Martin's taper-bushing installation sheet, in its published inch-pound units; it is not a universal value for every maker using the same series code. Confirm the supplied screw type and current component instructions before use. [S2]
Martin bushing series (extract)
Specified screw
Published wrench torque (in-lb)
1008
1/4-20 socket set screw
55
1610
3/8-16 socket set screw
175
2517
1/2-13 socket set screw
430
3030
5/8-11 socket set screw
800
Check on Martin's drawing
Installation
Removal
Hole purpose
Use the positions marked for installation
Use the separately marked removal positions
Thread engagement
Match the hole pattern; each completed hole is threaded on one side only
Do not assume both halves are threaded or that a vacant hole is an extra clamp position
Screw action
Prescribed screws establish the assembled clamp
Designated screws release the taper
Information to retain
Maker, series, matching hub, screw and specified torque
Maker's removal diagram and full safety instructions
This table identifies functions; it is not a complete maintenance procedure. Isolate the drive and use the exact component's installation/removal instructions and prescribed tools under a competent maintenance person. Do not generalize lubrication, heating, hammering or use of a drift across bush families. Martin specifically warns that anti-seize on the tapered cone or mounting-bolt threads can damage the mating component. A seized or damaged assembly needs manufacturer-directed assessment rather than improvised force. [S2]
For a supplier support request, provide the maker and complete part code, hub identification, finished bore, a clear view of the hole markings and the instruction revision. Ask the supplier to identify the installation and removal positions on that drawing. A photograph without the hole legend is not enough to resolve a disputed assembly. Keep the marked drawing with the maintenance record so future replacements are checked against the same identified system.
Chapter 4 / 06
Materials and Standards
The default material for a taper bush is grey cast iron, almost universally grade GG25, also designated EN-GJL-250 in the modern EN system. This iron has a hardness in the region of 220 HB and a minimum tensile strength near 250 N/mm2. It is chosen for three reasons: its flake-graphite microstructure damps the vibration that any belt or chain drive generates, it machines to a precise taper and clean keyway without the gummy chatter of low-carbon steel, and it is inexpensive at the casting volumes the industry produces. Bushes are usually finished with a black phosphate coating that gives mild corrosion protection and a uniform appearance.
Grey iron has limits. Its low impact toughness means a sudden shock or a careless hammer blow can crack it, and it is unsuitable for highly corrosive or washdown environments. For those duties manufacturers offer alternative grades, summarised below. Ductile (nodular) iron trades some damping for far higher impact resistance; steel bushes suit high-shock and reversing drives; and stainless steel covers food, pharmaceutical, and marine washdown service where the black phosphate finish would fail.
Separate the bush system from the keyway standard. BSI identifies BS 4235-2:1977 as a specification for Woodruff keys and corresponding keyways. It does not define Taper-Lock bush lengths, tapers or screw patterns. Confirm bush compatibility through the actual system drawing, and specify the keyway requirements separately on the order. [S1]
A matching finished bore does not by itself prove that the shaft key, keyway or hub seat matches. State the drawing's dimensional system and keyway specification separately from the bush series. For replacement work, retain the specified editions and check actual dimensions and tolerances; historical references such as ISO/R 773 should not be used as an automatic conversion between systems.
Shaft diameter, surface condition and the matching hub seat must satisfy the selected product's instructions. An oversized, damaged or contaminated interface can prevent correct assembly. Do not infer an acceptable fit, a mandatory flange gap or a universal shaft tolerance from appearance; obtain the maker's dimensional requirements for the exact bush and component.
Chapter 5 / 06
Key Specification Parameters
A taper bush is a deceptively simple part, but a handful of parameters fully define it for ordering and engineering. The decisive ones are the series code, the finished bore, the keyway standard, the bore range of the series, the rated cap-screw torque, the material grade, and the maximum permissible component speed. Each is decoded below.
Series code (four digits) is the primary identifier. The first two digits approximate the maximum bore and the last two the bush length, both in the original inch-and-tenths convention, so a 1610 is about 1.6 inch maximum bore by 1.0 inch long and a 2517 is about 2.5 inch maximum bore by 1.7 inch long. The code is constant worldwide regardless of whether the bore is machined in metric or inch units. Treat the digit arithmetic as a guide only and confirm the actual bore range against the maker table.
Finished bore and bore range establish which shafts the selected maker's series supports. Read the actual minimum and maximum bore and associated keyway data rather than deriving them from the series digits. Check the finished bore, wall section and mating hub as one assembly; a nearby available size is not a confirmed substitute.
Series
Approx. shaft range (mm)
Typical duty
1008
9 to 25
Compact light drives
1210
14 to 30
General duty
1610
14 to 42
Common belt and chain drives
2012
20 to 50
Medium torque
2517
25 to 60
Heavy-duty hubs
3020
30 to 75
High torque
3535
35 to 90
Large diameters
4040
40 to 110
Oversize shafts
Keyway and screws distinguish otherwise similar parts. State the finished bore, keyway drawing or standard and edition, screw type and thread, quantity and installation torque. Confirm each against the selected bush and mating component. Screw tightening torque must not be confused with rated drive torque. [S2]
Number and size of screws follows the size. Most common sizes use two cap screws and a third empty hole that doubles as the jacking position, so two screws are supplied. Larger sizes from roughly the 4030 upward use a four-hole pattern and are supplied with three screws, the logic being the same: one position is always vacant for extraction. Material grade should be matched to the duty per Chapter 4, with GG25 grey iron as the default and ductile iron, steel, or stainless reserved for shock, reversing, or corrosive service.
Maximum speed is a property of the assembled component rather than the bush alone, but it bounds the application. Cast-iron taper-bored pulleys are commonly rated to peripheral speeds around 30 m/s; above that the pulley itself, not the bush, becomes the limit, and balanced or steel components are needed. For high-speed fans and blowers, confirm the pulley speed rating and request dynamic balancing.
Chapter 6 / 06
Selection Decision Factors
Selecting a taper bush is mostly a matter of matching the component, the shaft, and the duty in the right order. Most errors come from deciding the bore before deciding the series, or from ignoring the keyway standard. The ordered checklist below works as a fixed selection and RFQ template.
Confirm the component system. Identify the actual maker, bush family, series and mating pulley, sprocket or coupling. Similar-looking Taper-Lock, QD and proprietary systems are not automatically interchangeable.
Select the series by torque and shaft. Choose the smallest series whose bore range comfortably contains the shaft diameter and whose rated capacity covers the transmitted torque with margin. A 1610 suits small motor drives; a 2517 or 3020 suits medium gearbox and conveyor duty.
Fix the finished bore. Order the exact bore and verify the shaft dimensions and surface condition against the selected product's drawing.
Specify the keyway. Retain the required dimensional system, standard edition and groove details from the shaft and hub drawing. Do not assume an inch and metric keyway become equivalent through a converted bore diameter.
Choose the material grade. Default to GG25 grey iron. Upgrade to ductile iron or steel for shock and reversing loads, and to stainless steel for food, pharmaceutical, or marine washdown environments.
Check the duty. Verify speed, torque, environment and material suitability for the selected complete assembly rather than applying a generic cast-iron or keyless-bush capacity.
Plan maintenance access. Retain the manufacturer's installation and removal diagrams, make the designated screw positions identifiable, and specify the approved screw and torque information on the work order. [S2]
Verify replacement compatibility. Compare the actual drawings and fastener requirements before qualifying a second supplier. BS 4235-2 is not evidence that all bushes of a nominal series interchange. [S1]
Keep the mating hub identification, bush series, finished bore, keyway drawing and approved fastener data with the spare-part record. This makes a future replacement check reproducible and reduces the risk of substituting an apparently similar bush with a different screw or seating arrangement. Availability and service support should be checked with the selected supplier rather than guaranteed from a standard number.
FAQ
What does a taper bush number such as 1610 or 2517 mean?
A number such as 1610 or 2517 identifies a series, not the complete shaft connection. Order it with the finished bore, keyway, maker and compatible mating component. Use the supplier's actual drawing and bore table; do not approve cross-brand interchangeability from the digits alone. BS 4235-2 is a Woodruff-key specification, not proof of taper-bush equivalence. [S1][S2]
What is the difference between a Taper-Lock bush and a QD bushing?
Both are split tapered sleeves clamped by cap screws, but the geometry differs and they are not interchangeable. A Taper-Lock bush has a single split through the wall and the taper runs the full length of the through bore, giving a compact flangeless fit. The screws thread alternately into the bush or the hub depending on whether you are installing or extracting. A QD (Quick Disconnect) bushing carries a flange on its outer end, splits through both flange and taper, and is bolted axially against the hub face. QD types are easier to remove and rebolt for frequent changeovers, while Taper-Lock gives a slimmer, lower-cost mount. QD follows the AGMA and ANSI tradition with series codes JA, SH, SDS, SD, SK, SF, E, and F.
What taper angle does a Taper-Lock bush use?
Use the selected maker's system drawing for taper dimensions and any angle definition. A general guide must not derive a universal bush taper from BS 4235-2: that standard concerns Woodruff keys and keyways. Matching geometry, bore, screw positions and component compatibility must be checked together before substitution. [S1]
How tight should the cap screws be torqued?
Use the current instruction sheet for the actual maker, bushing series, mating component and screw. The Martin values in Chapter 3 are explicitly a limited manufacturer example, not a universal torque chart. Installation screw torque and transmitted drive torque are different specifications. Apply the prescribed installation method and inspection requirements rather than carrying a torque from another brand or screw type. [S2]
How do you remove a taper bush that is fitted on a shaft?
Identify the exact bush and mating component, then follow the manufacturer's removal diagram under a competent maintenance person. Martin's sheet distinguishes removal screw positions from installation positions; each completed hole is threaded on one side only. Do not assume that every vacant hole is a tightening position or improvise heat, oil or a drift as a universal release method. The full component instructions and drive-isolation requirements take precedence over a summary. [S2]
What material are taper bushes made from?
The standard material is grey cast iron, commonly grade GG25 (EN-GJL-250), with a hardness around 220 HB and tensile strength near 250 N/mm2, usually finished with a black phosphate coating for corrosion resistance. Grey iron is chosen because its graphite structure damps vibration and machines cleanly to the precise taper. For high-shock duties, marine service, or stainless shafts, ductile iron and steel bushes are offered, giving higher impact resistance at greater cost. Stainless steel taper bushes exist for washdown and food-grade environments. The mating pulley or sprocket bore is also cast iron to GG25 or steel, machined to the matching taper specified by the component maker.
Which standards govern taper bushes?
The bushing's own system drawing establishes its required geometry and fastener arrangement. BS 4235-2 covers Woodruff keys and keyways; it is not a universal taper-bush sizing or interchangeability standard. Specify the shaft keyway separately, including its dimensional system and drawing requirements, and confirm that the actual bush fits the selected hub and shaft. [S1][S2]