Autoclaved aerated concrete (AAC) has a bulk density around 400-700 kg/m³ and a compressive strength typically in the 3-5 N/mm² range, with the material's cellular pore structure acting as the main reason generic wedge or sleeve anchor ratings never translate into the field [S3][S5].
A wedge anchor rated for 1,000+ lb ultimate pull-out in 4,000 psi (≈27.6 N/mm²) concrete depends on substrate confinement to generate expansion preload, and AAC does not provide that confinement. Published pull-out values for a 1/2" wedge anchor in normal-weight concrete can exceed 1,000 lb ultimate, while the same fastener in hollow CMU block typically falls into a much lower bracket and the failure mode shifts from steel fracture to substrate blow-out [S4][S5].
Why AAC Rejects Generic Masonry Anchor Ratings
Substrate density is the first filter: a 1/4" concrete screw commonly lists a 150-250 lb safe working range on poured concrete, but that figure is calibrated to dense substrates and drops sharply on porous block [S4].
AAC is a cement-bound aerated block with 60-80% air by volume, so expansion-type anchors split the cell wall instead of locking into it, and the head often pulls through the face shell under a sustained shear or tension load [S3]. Industry anchor selection guides segment substrates into concrete, brick, block, and tile, and explicitly call out CMU block as a case where only anchors that grip or toggle behind the hollow area should be used, which is the same logic that applies to AAC's voids [S3][S2].
Light-duty masonry anchors are commonly described as suitable for wall hangings up to 50 lb, and medium-duty up to 200 lb, but these buckets are calibrated to normal-weight substrates and must be discounted further on AAC because the substrate, not the fastener, is the weak link [S1].
Anchor Families That Actually Work in AAC
Three families consistently show up in AAC manufacturer guidance and structural fastener literature for aerated concrete: chemical (adhesive) anchors with screen sleeves, plastic/nylon frame anchors purpose-rated for aerated concrete, and helical AAC screws. [S2]
Chemical anchors with a screen tube or sleeve confine the resin in the borehole and bond the threaded rod to the AAC cell wall, with the bond area governed by embedment depth rather than mechanical interlock. Threaded-rod adhesive systems are the standard recommendation for overhead and high-load applications on masonry substrates in anchor selection guides [S2]. Plastic and nylon frame anchors rated for aerated concrete expand in a controlled way that does not burst the cell, and helical AAC screws cut a coarse thread into the aerated matrix, giving an immediate mechanical lock. For very heavy fixtures, cast-in-place anchors installed during AAC panel placement remain the highest-capacity option, but they require planning the location before the wall goes up [S2].
Comparison: Anchor Options on AAC at a Glance
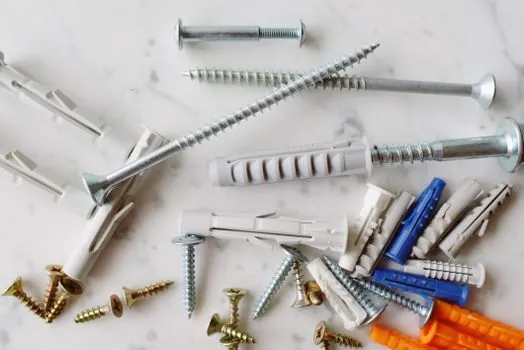
The three viable options trade off against four decision criteria: ultimate load capacity, install tolerance (retrofit vs planned), sensitivity to hole cleaning, and suitability near edges or in thin panels. [S3]
Chemical (adhesive) anchors with screen sleeves score high on capacity and edge-distance tolerance, score medium on install tolerance because they tolerate slightly oversized or wet holes, but score low on hole-cleaning tolerance: dust in the bore dramatically reduces bond, and the resin cure time becomes a schedule constraint [S2][S3]. Plastic/nylon frame anchors rate low to medium on capacity, high on install tolerance because they are the simplest retrofit option, medium on hole cleaning, and high on edge distance because they exert low expansion pressure. Helical AAC screws rate medium on capacity, high on install tolerance, high on hole cleaning because the cutting action clears dust, and medium on edge distance. Cast-in-place anchors rate the highest on capacity, but are effectively zero on install tolerance since the position must be coordinated before the panel is lifted into place [S2].
Sizing Rules and Safety Factor Practice
Published manufacturer tables for AAC anchors usually state an "allowable" or "recommended" load that already carries a 3:1 to 4:1 safety factor on the ultimate test value, and the same conservative ratio is the standard guidance in concrete-anchor selection references [S2].
As a working rule, a chemical anchor with a 100 mm embedment in AAC commonly lands in a 30-50 kg per-anchor working-load band, but the manufacturer table for the specific resin and rod diameter is the only number an engineer should submit, and the safety factor must be re-checked for sustained versus seismic loading. For dynamic, vibratory, or overhead loads, the conservative move is to drop the working load by an additional factor, or specify redundant fixings so that any single anchor failure is not catastrophic. Standard light-duty anchors in the 50 lb class and medium-duty in the 200 lb class should be treated as a starting envelope only, not a guarantee, on AAC [S1][S2].
Failure Modes You Can Pre-empt
Pull-out of the anchor head through the AAC face shell is the most common failure on expansion-type fasteners because the foam-like matrix crushes locally rather than gripping. [S2]
Bond failure at the resin/AAC interface is the dominant failure mode for under-cleaned chemical anchors, and a wire brush plus compressed air blow-out before injection is a non-negotiable step [S2]. Edge splitting shows up when anchors are placed too close to panel edges or to the joints between AAC blocks, and the simple mitigation is to respect the manufacturer edge-distance table, which on AAC is typically 100-150 mm for chemical anchors. Over-torquing during installation is a silent killer on aerated concrete, because the material yields locally and the clamp load decays, so a torque-limiting driver or a hand finish is worth the extra minute on every fixing. For a broader look at pull-out mechanics on a related substrate problem, see the short expansion anchor length analysis.
Spec Workflow for a Heavy Fixture on AAC
Start with the fixture's service load, then apply the safety factor, then pick the anchor family, then confirm embedment and edge distance against the manufacturer's AAC table, then verify with a site pull-out test on the actual panel lot. [S3]
The order matters because reversing it is how most AAC anchor failures happen: the specifier picks a familiar concrete anchor, looks up a tempting ultimate load, and never checks that the AAC substrate can develop that load. A site pull-out test on the delivered panel, using the same drill bit diameter and cleaning procedure, costs far less than a fallen HVAC unit or a failed fire-sprinkler drop, and it is the only way to confirm that the published allowable load is achievable on the material that actually arrived on site [S2][S3]. Specifying a chemical anchor for the heavy loads and pairing it with an AAC block wall assembly that the contractor can actually drill clean is the more reliable path than reaching for a wedge anchor that the substrate cannot hold. For lighter trim and accessories, expansion anchor products in plastic/nylon or helical-screw form remain the practical retrofit answer.