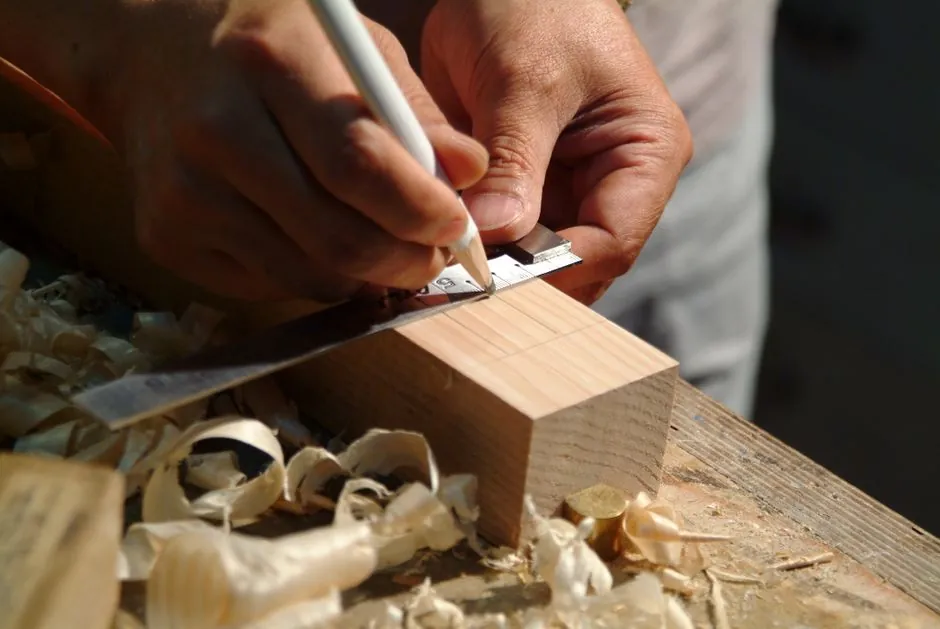
Central length is the length of a gauge block at the centre of its measuring face; variation in length is the maximum difference between that central length and the four corner measurements on the same face [S1][S2].
The two parameters are measured independently, calibrated separately, and they fail on different defects. PTB calibrates both interferometrically and only treats a block as in-tolerance when central length and variation in length are each within their stated bounds [S3].
What central length actually is
Central length (l_c) is the perpendicular distance between the two measuring faces measured at the geometric centre of the face, at 20.0 °C reference conditions with 101,325 Pa barometric pressure, 1,333 Pa water vapour pressure, and 0.03 % CO2 [S5].
Most laboratories measure the centre plus the four corners and then average or take the centre value; the four corner readings are kept separately because they feed the variation in length calculation [S1][S2]. For gauge blocks above 500 mm up to 1000 mm, the RISE national laboratory in Sweden measures only the central length, because the geometry contribution becomes small relative to length uncertainty [S8].
What variation in length actually is
Variation in length is the range of the four corner deviations from the central length, on a single face. NIST calls this the parallelism term, and it is the parameter that catches a block whose measuring face is not flat or whose two faces are not parallel [S1][S7].
For steel, ceramic, and tungsten carbide blocks up to 100 mm, NPL performs a visual inspection or calibration of measurement-face flatness and variation in length, in parallel with the length calibration [S4]. A block can pass central length but fail variation in length if a corner is proud, which is exactly the failure mode the corner measurements are designed to catch [S2].
How the two parameters are calibrated side by side
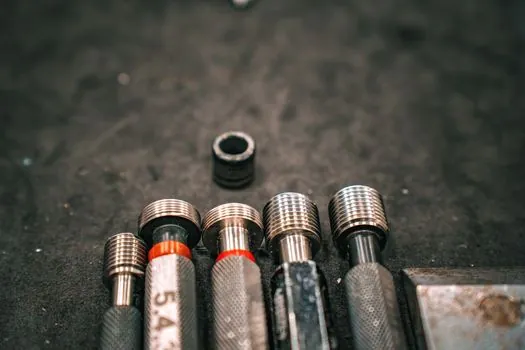
PTB's interferometric service measures both quantities simultaneously: if the measurement uncertainty and the stated tolerances for central length and variation in length are of the same order, the block is judged on both, not on a single combined number [S3].
NPL's workflow is similar: absolute interferometric calibration of central length (lower uncertainty) is used up to 100 mm; over 100 mm the central length is calibrated by comparison against a known standard; variation in length (parallelism) and flatness are calibrated as a separate deliverable on the same service order [S4]. The deliverable for a gauge block therefore typically lists two numbers per face plus a flatness figure, not one.
Grades, tolerances, and the per-parameter failure bands
ISO 3650:1998 (re-issued as BS EN ISO 3650:1999) defines tolerance grades K, 0, 00, and 1, with grade K being the tightest calibration grade and grade 1 the loosest workshop grade; ASME B89.1.9:2002 uses the same letter convention in inch units [S4].
Within any grade the standard sets two independent limits: the maximum permissible deviation from nominal central length, and the maximum permissible variation in length between the centre and any corner [S7]. MSC Direct's grade summary states explicitly that each grade "defines the allowable deviation from nominal length as well as the allowable variation in flatness and parallelism within a single block" [S7]. The two limits are not interchangeable: a block at the very edge of its central length tolerance can still be in grade if variation in length is tight, and vice versa.
Decision matrix: which parameter should drive a rejection
Use this four-criterion matrix when a block fails one of the parameters and you have to decide whether to send it back for re-calibration or scrap it. [S1]
NPL lists this as a routine service on grades K, 0, 00, and 1 [S4].
Failure mode B, variation in length excess (centre is in tolerance but one or two corners read high or low): investigate face damage, wring film contamination, or parallelism loss, then re-lap or scrap. Central-length re-calibration will not fix it [S1][S2].
Failure mode C, both parameters out together on a long block (above 500 mm): the RISE rule applies, only central length is even measured at that length, so the variation in length number has to be assessed by mechanical sweep rather than full corner mapping [S8].
Failure mode D, flatness independently out: separate from both length parameters, this is a wrung-face contact problem and is reported as its own deliverable on an NPL or PTB certificate [S3][S4].
Why the two are often confused on a shop-floor certificate
The confusion comes from a typical ISO 3650 certificate listing a single "deviation from nominal" line that is actually the central length result, while the variation in length is buried one or two columns over and expressed as a separate tolerance window [S6][S7].
The MMScience calibration paper restates the rule plainly: "Variation of length is a controlled parameter and in the case of the central length it is the variation in central length. Deviation from flatness is another" controlled parameter [S6]. Three controlled numbers, not one, are sitting on the certificate for a gauge block at grade K or 00.
What to check before signing a calibration certificate
Verify that the certificate reports central length, variation in length, and flatness as three separate lines, with a coverage probability of 95 % and an explicit k-factor or expanded uncertainty term [S3][S4].
Cross-check that the grade stated matches ISO 3650:1998 / BS EN ISO 3650:1999 (metric) or ASME B89.1.9:2002 (inch) and that the uncertainty quoted is consistent with the calibration method, absolute interferometry below 100 mm giving lower uncertainty than comparison above 100 mm [S4]. For an accredited certificate the UKAS lab number 0478 (NPL) or the equivalent PTB accreditation should be visible, and the traceability chain should resolve to the national standard of length [S4].
If only one number is reported for a gauge block at grade K or 00, ask the lab to re-issue; a single-number certificate does not meet the three-parameter minimum that ISO 3650 calls for [S6][S7].
For the relevant spec sheets and selection criteria, see aac block, and block brick.
This topic is covered further in A48 vs A536: Gray Iron and Ductile Iron Grade Selection Map.