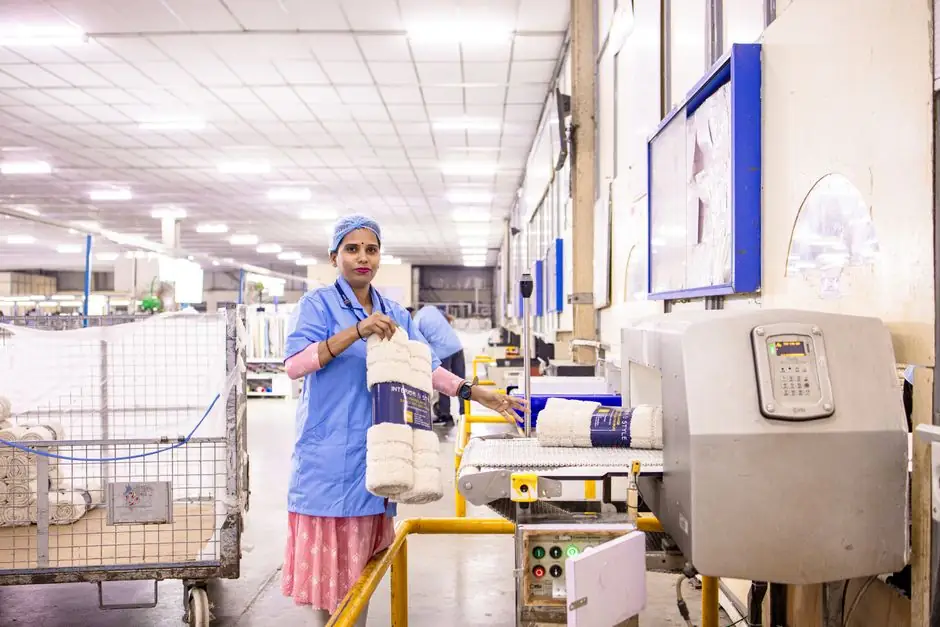
Checkweigher belts use load-cell conveyors of different lengths so packages can keep moving throughout inspection without delays [S4].
Product pitch, defined as the distance between successive packages, must be matched to the weighing zone, product length, line speed and reject mechanism rather than treated as a fixed gap [S2][S4].
What Minimum Product Spacing Means
Minimum product spacing is the smallest permitted longitudinal separation between packages, expressed as pitch or as an end-to-end gap, that prevents two products from influencing the same weighing result [S2].
Pitch should be checked across the complete dynamic system rather than only at the load-cell section. The load-cell conveyor length affects maximum product length and product spacing, while product orientation also affects how much belt area each item occupies [S4]. A wide belt or a small belt relative to the product can produce false readings or incorrect line spacing [S4].
Pitch, Gap and Line Speed Controls
Pitch is the distance between two packages as they are delivered to the checkweigher, while the package spacing gap is the clear separation between those packages [S2]. These terms describe different geometry and must be stated separately in an equipment specification.
Three values should be controlled together: product length, minimum pitch and belt speed. If speed rises without increasing pitch, the interval between product centres becomes shorter in time and the next item can enter before the controller has completed recognition and classification [S2][S4].
The practical comparison is straightforward:
Gap-only spacing is easy to specify but leaves product length unstated. Full pitch is safer for layout control because it defines the centre-to-centre footprint of each package [S2].
The complete specification should record minimum end-to-end gap, minimum centre pitch, maximum product length, maximum product width, line speed and belt length. It should also identify whether products may touch, whether a fixed spacer or singulation device is required, and how acceleration and deceleration affect pitch variation.
Belt-Selected Systems Versus Fixed-Pitch Systems
Fixed-pitch systems suit long, uniform packages on controlled lines because product position is regular and the required belt geometry can be calculated directly [S2][S4]. The limiting factor is whether the conveyor can physically hold the selected pitch while the product is recognised, weighed and classified.
Variable-pitch systems use product recognition, separation or upstream control to establish spacing before weighing. This is more suitable for mixed or moving products, but the rejection method and downstream transfer must still provide enough separation to prevent one rejected item from disturbing another [S2].
For direct comparison, fixed-pitch equipment offers simpler geometry, a shorter specification cycle and predictable belt sizing.
Neither arrangement removes the need for an acceptance test. Package length and weight distribution vary in real production, and a nominal gap cannot guarantee stable measurements if the upstream conveyor allows products to rotate, overlap or enter at inconsistent speeds [S2][S4].
Accuracy Classes, Sensing Technology and Rejection
Those figures describe sensing capability, not the tolerance created by poor spacing. If products enter the weighing zone together, impact forces, overlapping footprints and signal transitions can prevent the scale from resolving each item as an independent transaction.
A visual or audible indication identifies a product within the target range, while an overweight or underweight result can trigger rejection or diversion [S5]. Common reject methods include a push-off arm and a blast of air [S4]. Rejection hardware requires downstream space because the rejected package must move away from accepted product without creating a new collision or overlap condition.
For accepted-product documentation, the checkweigher records the measurement target, weight zones and reject action. A filling-weighing-scale may supply feedback to the filler, but that closed-loop function does not replace proper infeed spacing.
Where Spacing Becomes a Quality-Critical Requirement
Packaged food and pet food commonly move through dynamic checkweighers, and applications extend from a few grams to more than 20 kg [S1]. Heavy 50 lb bags are also identified as suitable checkweigher loads where X-ray inspection has difficulty resolving the package [S6].
The economic stakes rise with line volume. A line processing 120 granola-bar packs per minute produces about 57,000 packs per shift; an average 5 g overfill at $0.05 per pack adds $85,000 per month, while reducing overfill by 2 g saves nearly $35,000 per month [S1].
Pharmaceutical use raises the quality threshold further. A 0.5 mg deviation from a labelled tablet, capsule or vial weight can indicate inaccurate active-ingredient dosage and can affect treatment efficacy or cause adverse effects [S1]. Spacing must therefore preserve individual-item resolution rather than merely maintain line rate.
Checkweighers can also inspect complete cases for missing cartons, bottles, bags or cans, and verify package counts by weight [S2]. If spacing is insufficient, a case-count application can create false count alarms that resemble missing components.
Sizing, Validation and Failure Modes
The primary design rule is concrete: weighing-belt length must be at least 1.5 times product length, with product orientation and load-cell conveyor length also controlling maximum spacing requirements [S4]. Belt widths cited in equipment guidance range from under 3 inches, through 3–6 inches, to larger sizes, and the correct width must match the package footprint [S4].
Three failure modes deserve separate tests. First, insufficient pitch causes product overlap or premature entry. Second, incorrect belt width can produce false readings or incorrect spacing [S4]. Third, mechanical disturbance around the load cells, including air movement or applied force, can cause false readings [S4].
Validation should use the longest and lightest expected product, the heaviest expected product, the intended line speed and the worst credible infeed variation. The test should record 100% of production rather than intermittent samples because a checkweigher provides complete-item inspection [S2].
Statistical evaluation should include standard deviation, weight-zone distribution, total count, total weight and production speed [S2]. Acceptance should also include confirmation that every underweight, overweight or missing-component event is rejected correctly and that rejected goods do not re-enter the accepted stream.
For heavier packages, selecting a case checkweigher for 25 kg shipping loads adds capacity, frame and infield considerations. Capacity selection cannot compensate for a pitch that causes two 25 kg loads to be measured as one event.
Procurement Specification and Acceptance Test
A purchase specification should state the minimum pitch as a controlled dimension, not as “adequate spacing.” It should list product length, product width, product orientation, maximum line speed, minimum gap, weighing-belt length and reject type as a coordinated set [S2][S4].
For example, a 300 mm carton on a 100 mm pitch occupies a 400 mm footprint before a clear gap is added. A 450 mm minimum weighing belt meets the 1.5-times-product-length rule, but it does not prove that a 100 mm pitch is sufficient at the proposed speed [S4]. The manufacturer must validate recognition, isolation and classification for the complete combination.
The factory acceptance test should run 100 consecutive units through the intended spacing, inject known underweight and overweight samples, and confirm correct sorting [S2]. It should repeat at minimum, nominal and maximum line speed and with the longest product presented in each approved orientation.
For acceptance, record the number of misclassified units, reject false-actuation count, average pitch, minimum pitch and maximum pitch. The controller should also preserve weight-zone settings and production statistics for management and regulatory records [S2].
The trackable commissioning signal is a stable pitch trace with no overlapping footprints and a defined minimum gap in every approved product orientation. A second signal is zero classification errors during the 100-item acceptance test. If either fails, adjust the infeed, lengthen the weighing section or revise the line speed before loosening the weight limits.