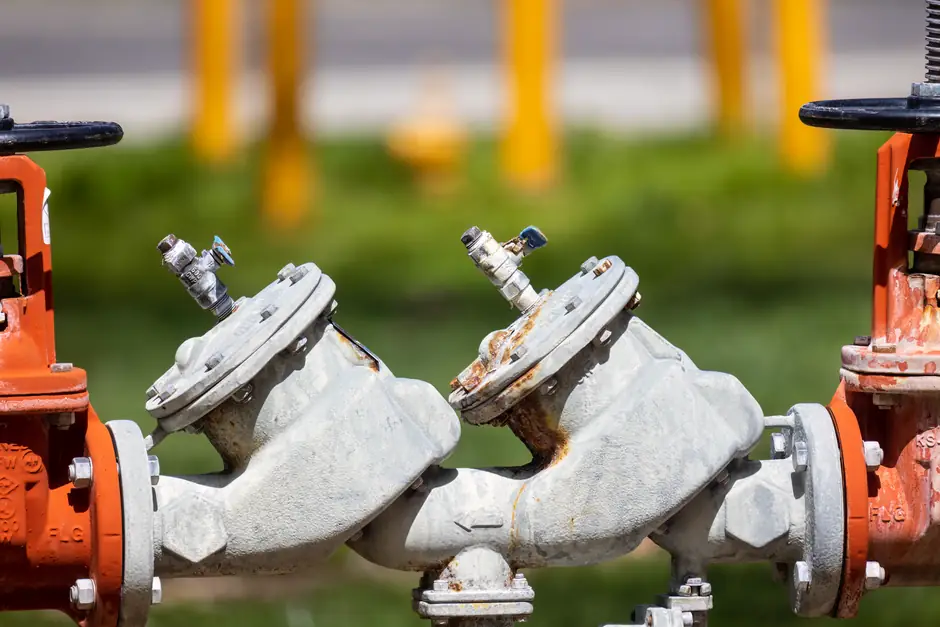
Select a gate valve for pulp and paper isolation when the service requires full-open or full-close operation, a straight flow path, and resistance to fibrous or abrasive stock.
The decision is not a single material call: a knife gate suits pulp slurry, a wedge gate suits cleaner or more pressurized service, and a butterfly valve may win where quick quarter-turn closure and lower weight matter more than a gate's dirt tolerance [S1][S9].
Define the valve duty before comparing designs
Pulp and paper mills contain several distinct service classes: chip feed, pulping, stock preparation, bleaching, chemical recovery, paper-machine chest, recycle, rejects, and effluent. Each class carries a different combination of pressure, temperature, chemistry, consistency, fiber content, solids concentration, and operating frequency [S3].
A valve used only for isolation should not be asked to modulate flow. Gate valves are intended primarily for on/off service because they move from a wide open to a wide closed position slowly, while their straight-through bore reduces pressure loss and limits fiber accumulation [S1]. They are not suitable for throttling, and a gate installed in a control loop can create unstable process behavior [S4].
The comparison below organizes the main gate-valve choices around four decision criteria:
For a detailed treatment of ball valve selection for pulp and paper stock, trim, and seat choices, use rotary valves only where their control range, seat design, and torque requirements match the specified process condition.
Use knife gates for fibrous stock and severe isolation duty
Knife gate valves are used for on/off isolation in pulp-and-paper recycle and rejects because the moving blade can cut through fibrous media that can lodge on a conventional gate seat [S6]. A knife gate is therefore a practical default for stock lines, sludge, pulp, and recycle service, but it is not a universal solution for clean high-pressure steam or for throttling [S9].
DeZURIK identifies cast and fabricated knife gate valves for a broad range of mill media and applications, while Bray Series 942 valves are specified for on/off isolation in recycle and rejects service [S6][S7]. The design feature to confirm is not simply the presence of a knife, but whether the blade, seat, body, stem, packing, and actuator form a package suitable for the actual pressure, temperature, chemistry, and cycle demand.
For paper-stock control, an O-port gate valve is recommended because its flow passage removes a section of the pipeline cross-section as the gate closes, reducing the obstruction that can retain fibers [S4]. The same geometry also explains why knife-gate performance degrades during closure: the pressure drop rises as the open area narrows, and the seat must remain stable against the slurry [S4][S9].
The comparison is direct. A knife gate is stronger for cutting through fibrous solids and dirty isolation, a wedge gate provides a compact full-port isolation solution for cleaner service, and a butterfly valve offers quarter-turn operation with lower installed weight. For actuation speed, sealing, and test criteria, the knife gate and butterfly valve are compared by closure behavior, seat leakage, actuator sizing, and pressure testing [S9].
Match pressure, temperature, and material to the process zone
Pulp and paper service can include sodium hydroxide, sodium sulfide, chlorine dioxide, high-temperature steam, abrasive wood fibers, and silica-bearing solids [S1]. A valve body that handles one stream does not automatically handle the cleaning chemistry used for boil-out, scale removal, or biological growth, so material compatibility must be checked against both process media and cleaning chemicals [S4].
Valve selection data should identify the design pressure and temperature, pressure rating, body and trim material, seat and seal material, stem construction, end connection, allowable seat leakage, and actuator arrangement. The mill should also state consistency, freeness, scale tendency, fluid velocity, cycle frequency, operation speed, response accuracy, and maintenance access, because these are primary application criteria rather than optional notes [S4].
For abrasive service, the review must consider erosion of the body, trim, and closure member. A 2024 industry selection note identifies gate valves near the bottom of cyclones in applications involving Hastelloy, titanium, or Monel, while also identifying knife gates as bottom-valve configurations [S8]. These material and geometry choices need project-specific confirmation rather than blanket substitution, because the same source identifies the service as erosive and the selection depends on the installed condition [S8].
A rising-stem gate can expose the stem packing to a less severe thermal environment than a non-rising stem, but the packing, bonnet, stem material, and seat must still be compatible with the process. The source selection framework calls for leak-free packing, defined seat leakage, cycle duty, and inspection access [S4]. For steam service, the operating failure mode is especially relevant to why a gate valve fails at steam throttling, because thermal expansion and throttling force can distort a gate seat that is not designed for modulation.
Separate stock isolation from control and diverting duties
Gate valves are appropriate for isolation, not mixing, diverting, or continuous flow regulation. A globe valve is more suitable when the function requires throttling, while quarter-turn valves with hardened trim are used for steam and chemical control in pulping operations [S1][S3]. A check valve may instead be required where reverse flow could contaminate a line or damage a pump, such as bleach-plant feedwater and black-liquor service [S1].
The decision sequence should start with function: isolation, control, mixing, or diverting. Process conditions then determine pressure rating, temperature range, chemical compatibility, consistency, freeness, and scale tendency. Valve-operation criteria add packing leakage, seat leakage, operating frequency, fluid velocity, cycle duty, operating speed, and response accuracy, while installation criteria cover dimensions and maintenance access [S4].
That sequence prevents a common specification error: treating every quarter-turn device as equivalent. A butterfly valve can provide quick isolation in a large line, but it introduces a rotating disc into the flow path and requires seat, material, and torque checks. A ball valve offers a quarter-turn alternative where its bore, trim, seat, and control configuration suit the media. Neither conclusion removes the need to verify fibrous-media behavior, chemical compatibility, and pressure-temperature limits [S3][S9].
Specify actuation, testing, and maintenance access
Manual, pneumatic, hydraulic, or electric actuation should be selected from the required operating speed, cycle frequency, fail position, available force, and maintenance philosophy. A gate valve requires sufficient actuator torque to move the closure member through the pressure drop and, for a knife gate, through fibrous stock. Sizing must include the valve’s stated maximum differential pressure and media condition rather than using line pressure alone [S4][S9].
Isolation specifications should define allowable seat leakage, especially for low-pressure service, and should state whether double block-and-bleed is required for lockout or confined-space conditions. Fugitive emissions, manual-actuation ergonomics, packing-leak risk, and slip hazards around leaking media are also part of the mill safety review [S4]. For procurement review, request pressure-temperature, material, seat-leakage, actuator, and documentation requirements as separate line items.
Operation frequency matters because packing, seats, stems, and actuators all have different cycle lives. The selection framework calls for partial-stroke or inline diagnostic testing where appropriate, together with an assessment of installation and maintenance access [S4]. A valve that must be removed from a congested pipe rack or a live digester or recovery system may have a lower practical service life than its laboratory cycle rating suggests.
Build the purchase specification as a service matrix
Each mill application should have its own valve data sheet. The minimum service matrix should include tag, line description, function, normal and maximum pressure, normal and maximum temperature, media composition, fiber or solids characteristics, flow direction, valve type, body material, trim and seat material, closure member, end connection, allowable leakage, actuator type, fail action, cycle frequency, coating requirement, inspection access, and cleaning chemistry [S4].
For fibrous stock, include the information needed to compare a knife gate with a butterfly valve: media, pressure, closure force, sealing performance, actuation, and test requirements [S9]. For stock-control applications, document the O-port geometry and the requirement to remove a cross-section of the pipeline as closure occurs [S4]. For recovery, bleaching, and steam systems, include the chemical concentration or composition, scaling tendency, temperature range, and cleaning procedure rather than writing only “pulp service.”
The final choice should pass 4 checks. First, it must provide the required function, isolation or control. Second, its pressure-temperature rating and materials must fit the process and boil-out chemistry. Third, its closure geometry must handle the fibers, solids, and erosion mechanism. Fourth, the actuator, test, leakage, and access requirements must support the real maintenance plan. That approach makes gate valve selection a traceable engineering decision instead of a preference based on a product family name.