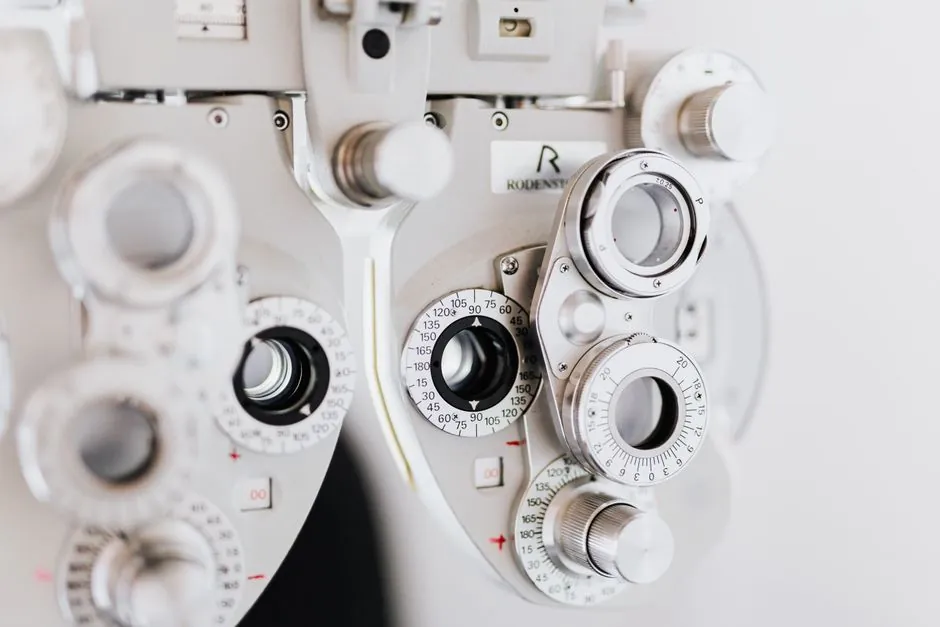
Overlay charts on a profile projector remain the quickest visual method for round-part radius work, because the operator aligns the projected shadow against printed concentric arcs and reads the radius value off the chart in a single view, with magnification up to 100x on current machines [S5].
On a horizontal benchtop unit the part sits on a 175 × 100 mm stage and a 340 mm screen, on a 23.6 in (600 mm) floor-standing comparator the stage expands to 450 × 200 mm, and overlay charts clip to the screen on all of these models [S5]. Radius measurement on the optical comparator can reach five ten-thousandths of an inch when magnification, focus, and a certified reference standard are all set per the manufacturer procedure [S3].
How a radius overlay chart works on the screen
A radius chart is a transparent or printed template carrying a family of concentric arcs at fixed radii, clipped to the comparator screen so the part's magnified shadow projects on top of it [S1]. The operator slides the stage until one edge of the arc on the part falls tangent to a chart arc, then checks whether the other edge of the same feature also falls tangent: if both sides kiss the same arc, the radius is correct; if the shadow grows or shrinks between the two tangent points, the part is out of round [S1]. The same chart family also gives concentricity, because the operator watches the gap between the shadow arc and the chart arc as the part is rotated on centers or a V-block [S4].
Step Radius Chart-Gages, where each 90° or 180° sector is divided into radii that step up in small increments, let the operator bracket an unknown radius between two adjacent steps and read the value by interpolation, without ever leaving the screen [S4]. Because the chart is dimensionally stable Mylar or glass with sharp, uniform line widths, the inspection is repeatable across operators and across shifts, which is the whole point of optical gaging [S8].
Why an overlay beats a hand-held radius gage for first-article roundness
An overlay chart lets the operator check radii, angles, lengths, and thread forms in a single fixture, because the comparator stage runs on 0.5 µm linear scales so the dimension is read from the scale and not from a hand-turned thimble [S5]. A handheld radius gage, by contrast, requires the operator to find the tangent point by feel on a flexible part, which is exactly the case where the part is a thin stamping, a rubber seal, or a small medical implant that deforms the moment a caliper jaw touches it [S5]. On those parts the comparator's zero-force shadow measurement is the only practical way to read the true radius [S3].
CAD-overlay software is now a drop-in replacement for printed charts on the same fixture: import the .dxf, scan the edge, and the readout best-fits the profile to CAD and marks every feature in or out of tolerance, so the chart and the software are interchangeable on the same screen [S5]. For a small radius range, however, the printed chart is still the faster visual pass, because the operator can sweep the silhouette against a fixed set of arcs in seconds, with no edge-detection latency.
Round-part inspection criteria: chart arc vs shadow arc
Three criteria decide whether a round feature passes: (1) both tangent points of the shadow arc must touch the same chart arc, (2) the gap between the shadow arc and the chart arc must stay within the print tolerance across the full 360°, and (3) the radius read from the stage scale must match the chart radius within the comparator's stated accuracy, which is on the order of 0.0005 in at typical 10x to 50x magnifications [S3]. For a 1.000 in radius on a 0.005 in tolerance print, that means the operator needs at least 20x magnification so the 0.005 in band projects to a 0.1 in visible gap on the screen, which is readable by eye on a 340 mm or larger screen [S5].
For features smaller than 0.005 in the comparison tightens: a 0.001 in tolerance at 50x projects to 0.05 in on the screen, which is near the visual limit, and that is the regime where a 0.5 µm linear scale on the stage, a calibrated reference standard, and CAD overlay software outperform a hand-held gage [S3][S5]. A plain Mylar radius chart with stepped arcs in 0.001 in increments is still usable, but only if the chart lines are sharp and uniform, which is why chart material (rigid substrate, stable humidity and temperature coefficients) is treated as a gage-class component rather than office stationery [S4][S8].
Material and environment: keeping the chart honest
Comparator chart-gages are dimensionally stable Mylar or optical glass, and the lines must be uniform in width with sharp edges so the visual comparison does not introduce a reading error larger than the part's tolerance [S4]. Mylar overlays in particular are popular because they are transparent, easy to swap, and tolerate routine cleaning, but they must be stored flat and never rolled, because a curled chart distorts the projected scale and gives a false radius reading [S8]. Humidity and temperature coefficients of the chart substrate must be matched to the shop environment, otherwise a chart that is accurate at 20 °C will drift in a non-climate-controlled QC cell [S4].
Surface illumination is required for parts that are not silhouette-friendly, such as a turned radius with a fine surface finish, and the comparator must have a surface light source in addition to the standard substage lamp; that is one of the inputs Gage-Line asks for when quoting a custom chart [S4]. For routine radii on turned shafts, a horizontal light path with substage illumination plus a V-block or centers fixture is the standard configuration, because it lets the operator rotate the part in place and watch the shadow arc sweep across the chart [S5].
Chart-gage selection for the radius range you actually inspect
For a small family of radii (say, a range of 0.030 in to 0.250 in), a step radius chart with arcs in 0.005 in or 0.010 in increments is the practical choice, because the operator can bracket the value and read by interpolation without leaving the screen [S4]. For a wide radius range (0.010 in to 2.000 in on turned shafts), a combination chart-gage that carries both a radius family and an angle protractor on the same overlay is the standard shop-floor choice, because the operator can sweep through radii and angle checks in a single setup [S4]. For thread forms, a dedicated thread chart-gage carries the go and not-go profiles plus a 60° protractor, which a plain radius chart cannot do.
For new work where the radius is not yet stable across revisions, CAD overlay on the FUSION-class readout is more economical than printing a new Mylar chart every print revision, because the chart is the .dxf and the chart material is the screen [S5]. For a fixed, high-volume radius that is the same part drawing for years, the printed Mylar chart is cheaper per inspection and runs on any comparator, including older horizontal units without a digital readout [S4][S8].
Where the overlay method breaks down
Overlay charts are silhouette-only: an internal radius that is not visible from the projected outline cannot be checked on a chart, and the part must be sectioned, or the inspection moved to a vision measuring machine that uses edge detection on a through-lens image rather than a shadow [S6]. Hidden features such as a bore radius behind a wall are out of scope for the chart, and a touch probe on a CMM is the correct tool there.
Sub-0.005 in features on a Mylar chart with 0.001 in arc steps are near the visual limit, and a CAD overlay with edge best-fit is the more reliable check, because the software can resolve sub-pixel deviations the eye cannot [S3][S5]. Part coatings or surface finishes that scatter the substage light also defeat the chart method, because the shadow edge becomes diffuse and the tangent point is no longer sharp; surface illumination with a fiber-optic ring light is the fix, but it only works on a comparator equipped for it [S4][S5].
Standards and sourcing notes for chart-gage work
Optical comparator inspection with overlay charts is a non-contact, comparative method, and the chart itself is treated as a gage with documented accuracy, not as a printed reference, so chart storage, handling, and calibration against a certified reference standard are part of the procedure [S3][S4]. Magnification, focus, and scale calibration must be set against a certified reference standard or gage block before any measurement is taken, and accuracy down to 0.0005 in is achievable when the procedure is followed [S3]. The chart substrate and its lines must be dimensionally stable, sharp, uniform in width, and stored flat, with humidity and temperature coefficients documented for the QC environment [S4][S8].
For a working metrology cell, the practical sourcing path is: pick the radius range and step size, decide between printed Mylar (cheap, fixed, no readout needed) and CAD overlay (flexible, requires a digital readout such as the FT2-E FUSION), and confirm the comparator has a 0.5 µm linear scale on the stage so the stage reading matches the chart reading within tolerance [S5]. The chart and the stage scale are the two gages; the comparator optics are the carrier.
Trackable next signal: whether your print's smallest radius is above or below 0.005 in decides chart step size and whether CAD overlay is required. Trackable next signal: confirm surface illumination is fitted on the comparator if any of the round features in scope are not silhouette-friendly.