Select a dedicated high-temperature chain oil when the operating chain temperature is high enough that general-purpose oil can volatilize, oxidize into deposits, or lose film strength; a documented product class with a 450°F upper temperature example is available for conveyor chains [S5].
The decision depends on five measurable variables: chain temperature, lubricant viscosity, flash point, evaporation behavior, and residue formation. High-temperature chain oils serve plasterboard, insulation, oven, and other heated conveyor or drive applications [S2].
High-Temperature Chain Oil or General-Purpose Oil: Selection Criteria
General-purpose oil is appropriate only when its operating-temperature rating, flash point, oxidation stability, and residue behavior cover the complete lubrication point. Renold states that, in most applications, a properly lubricated chain should last for at least 15,000 operating hours [S4].
High-temperature chain oil is the stronger choice when any one of four conditions applies: the chain runs above the general oil’s rated service range, evaporation loss shortens the relubrication interval, oxidation produces sticky residue, or the lubricant must resist drip-off from a moving chain. High-temperature oils must reduce friction and wear, penetrate the roller-bushing interface, remain adhesive enough to resist centrifugal loss, and leave a residue that can flow and redissolve [S2].
Do not select a lubricant by viscosity alone. Viscosity sets lubricant-film behavior, but penetration, adhesion, flash point, evaporation loss, and residue condition determine whether the chain remains protected between relubrication cycles [S2][S4].
Performance Comparison Across Four Decision Criteria
On operating-temperature capability, a general-purpose oil is simpler and less expensive where its rating is adequate, while a dedicated high-temperature chain oil is required for exposed heated chains. One commercial conveyor-chain range includes high-temperature oil with a 150, 124, or 514°F rating and a low-temperature limit of -27°F, although the exact rating belongs to the selected product rather than the entire category [S5].
On wear control, dedicated chain oil is preferable because the objective is not merely an external film. The critical friction points are between rollers and bushings, while an oil film on the outside surface mainly provides rust protection and reduces sprocket wear [S5]. A general oil can reach those internal surfaces only if it has adequate penetration and wetting behavior [S2].
On residue and fire risk, dedicated high-temperature oil wins when conventional oil oxidizes into carbonaceous deposits. Food-grade chain lubricants can sludge at elevated temperatures, and those deposits can block chain links [S6]. Oven-chain lubricants are specifically formulated to prevent residue buildup, penetrate narrow gaps, and reduce oven fire likelihood [S1].
On application control, a general oil may be adequate for an ambient chain, but a high-temperature chain oil can be selected with controlled viscosity and application equipment. The practical choice is therefore: use general-purpose oil only where its temperature and deposit limits are proven; use dedicated high-temperature chain oil where the chain sees sustained heat, contamination control matters, or residue can impede operation [S1][S2][S5].
Viscosity, Penetration, and Relubrication Interval
Chain viscosity must be matched to the machine rather than selected from a single “hot oil” description. The chain manufacturer also warns that heavy oils and greases may be too stiff to penetrate the working surfaces, while grease applied only outside the chain can act as a seal and increase wear [S4].
Penetration and adhesion are opposing requirements. High-temperature chain oil must penetrate between plates and into the roller-bushing region, yet remain attached long enough to resist drip-off. This balance becomes more important as viscosity changes with temperature [S2].
Relubrication frequency should follow measured evaporation and deposit behavior rather than a calendar assumption. Low evaporation loss supports longer intervals and reduces contamination of exhaust filters, while the remaining residue must remain smooth, flow between links, and redissolve in fresh oil [S2]. For a general-purpose oil, an oil reservoir or automatic industrial-lubricant system still requires verification at the hottest chain location, not only at the reservoir or nozzle.
Flash Point, Evaporation, and Fire-Risk Control
Maintain a safety gap between the lubricant flash point and the chain’s maximum operating temperature. High-temperature chain-oil performance must be evaluated for evaporation loss and residue formation because these properties directly affect relubrication frequency, filter contamination, and deposit blockage [S2].
Use the flash point as a selection limit, not a operating-temperature rating. A flash point above the chain temperature reduces ignition risk, but it does not establish oxidation stability, deposit behavior, or service life. Those properties require separate lubricant data and application testing [S2].
For testing, the cited high-temperature chain-lubrication method uses the Cleveland open-cup flash-point method, a four-ball test for extreme-pressure properties and wear, and SRV equipment for friction and wear under oscillating movement. SRV testing can simulate high-temperature applications up to 300°C (572°F) [S2]. Evaporation can be evaluated by a defined-temperature cup test or thermogravimetric analysis, which measures weight loss as a function of temperature [S2].
Oven applications require stricter housekeeping because lubricant mist, drip-off, and accumulated residue can increase fire exposure. Summit identifies its oven-chain products as high-temperature lubricants intended to reduce residue buildup and oven fire likelihood [S1]. Food-processing applications should additionally require an H-1 lubricant designation and supplier documentation appropriate to the process; one 450 Food Grade H-1 chain-lube technical line documents the performance concern at elevated temperature [S6].
Application Fit and Material-Specific Limits
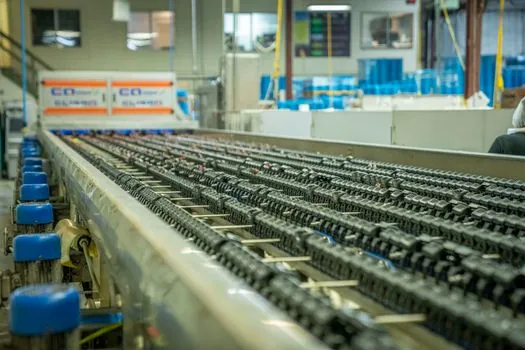
Specialized high-temperature chain oil is suited to oven chains, roller chains, conveyor chains, steel belts, heated press platens, and chains operating in extreme-temperature equipment. Named applications include bread, cookie, and cake ovens, gypsum ovens, fiberglass lines, rockwool production, and insulation-material handling [S1].
General-purpose oil is better suited to ambient or moderately heated chains where the fluid remains stable, penetrates the links, does not leave obstructive residue, and provides adequate film strength. General-purpose chain lubricants can offer anti-wear properties, lubricity, and stay-in-place behavior, but those claims do not replace temperature-specific qualification [S7].
Grease is generally a poor substitute for a fluid at elevated temperature when penetration into the chain is required. The chain manufacturer states that heavy oils and greases can be too stiff to reach the working surfaces, and repeated relubrication can build thick layers on plates and rollers that trap dust and increase the effective chain thickness [S4].
Do not assume that any high-temperature fluid is suitable for every conveyor-chain design. Check the chain maker’s lubricant type, viscosity, temperature limit, and relubrication method, then verify compatibility with seals, coatings, cleaners, and adjacent lubricants. The materials cited for industrial chains include plates, pins, bushes, and rollers, which means lubricant access and contamination behavior at each interface must be considered [S4].
Procurement and Acceptance Tests
Specify the lubricant by performance and operating limits, not only by the label “chain oil.” A procurement request should include the chain type, minimum and maximum chain temperature, ambient temperature, load, speed, lubrication point, relubrication method, contamination exposure, and acceptable residue condition. Relevant data include viscosity at a stated test temperature, flash point, evaporation loss, application compatibility, and any food- or fire-safety classification [S1][S2][S6].
Use a one-line comparison during approval. General-purpose oil wins on simplicity when temperature exposure is modest. General-purpose oil loses when its flash-point margin is inadequate or it leaves deposits. A dedicated chain oil wins when high-temperature stability, penetration, and residue control are critical. A grease loses when the design requires repeated penetration into roller-bushing contacts [S2][S4].
Before release, run an application-specific acceptance check. Confirm lubricant delivery into the working gap, inspect residue after the intended relubrication interval, monitor chain wear and elongation, and verify that the lubricant does not interfere with adjacent equipment. High-quality conveyor-chain oil can reduce chain stretch, while poor or insufficient lubrication is identified as the single biggest chain-failure risk factor in the cited chain-maintenance material [S4][S5].
The next control point is measurable: record peak chain temperature, lubricant consumption per lubrication interval, visible deposit condition, and chain elongation against the same baseline. If deposit accumulates, relubrication consumes more oil, or flash-point margin shrinks at the hottest zone, replace the general-purpose oil with a qualified high-temperature chain lubricant and repeat the check under actual service conditions [S2][S5][S6].