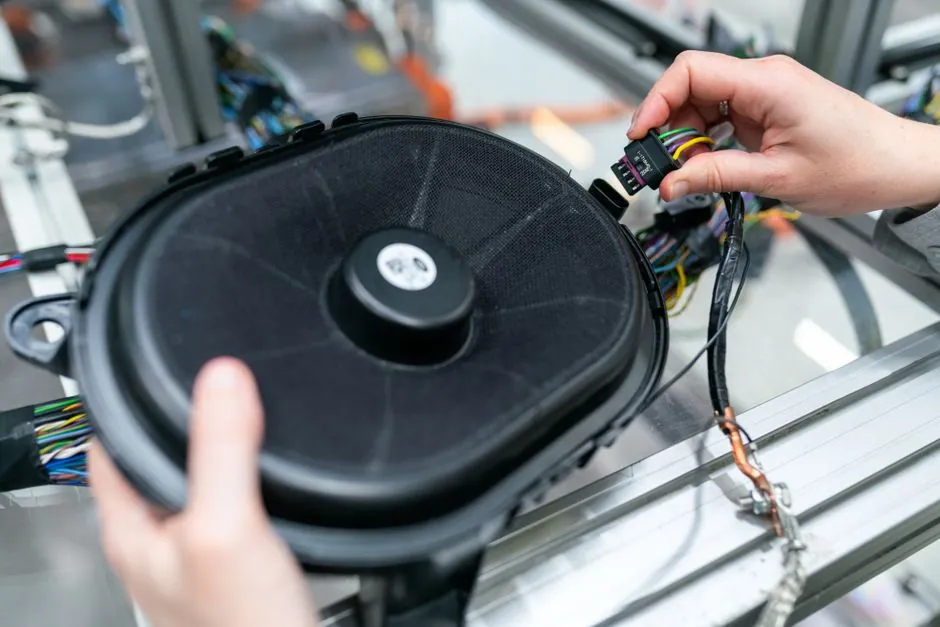
For a connector housing operated continuously at 150°C, specify a qualified PPS or LCP grade and verify creep, warpage, moisture, and assembly performance at that temperature [S1][S5][S6].
The decision must cover 150°C continuous exposure, any 200°C peak, SMT reflow at 260°C where applicable, dimensional retention, electrical performance, flame rating, and the required terminal-retention force.
PPS and LCP Fit the 150°C Duty
PPS is a suitable option for a heat-exposed housing because it provides dimensional stability and inherent flame retardance for high-temperature service [S5]. LCP is the process-selection alternative when thin walls and low warpage dominate, and it can survive a 260°C reflow peak [S5].
Both materials sit above the stated continuous-service boundary of 150°C. General engineering plastics such as POM, PA66, and PPS hold dimensional stability up to 180–260°C [S1].
The comparison separates continuous service from short-term heat deflection. A resin with an HDT above 150°C may still fail as a 150°C housing if creep, thermal aging, moisture uptake, or weld-line strength is not acceptable at the operating stress.
Define Continuous and Peak Temperatures
An automotive-style under-hood connector can face 125–150°C continuous exposure and peaks above 200°C, while a passenger-compartment connector may operate from -40°C to 85°C [S2]. Specify the actual thermal profile before choosing a grade: 150°C continuous for 10,000 hours is materially different from 150°C for 1 hour or 200°C for short peaks.
The candidate housing must retain geometry, latch function, terminal normal force, and electrical insulation across the full profile. Connector polymer failures include creep and stress relaxation under sustained load, latch fatigue, weld-line weakness, blistering, delamination, and warpage [S3].
Place gates and knit lines away from latch roots and terminal-support shoulders, then validate those locations after molding. A 0.01 mm dimensional tolerance can be cited as the demanding connector case identified for 260°C reflow, but an actual housing must be evaluated against its own tolerance stack [S5].
Choose Between PPS, LCP, and High-Temperature PA
PPS is the preferred candidate when 150°C continuous operation is combined with creep loading, chemical exposure, or dimensional stability. LCP is the preferred candidate for thin-wall, low-warpage housings requiring SMT reflow; connector applications include high-speed USB and micro-pitch board-to-board interfaces [S5]. High-temperature PA is appropriate when toughness, repeated mating, and low moisture absorption matter more than the lowest warpage [S5].
PA66 is a mainstream molded-connector material, but its published continuous-use limit is 130°C, and PA66 is listed at 120–150°C in a broader material matrix [S1]. It therefore leaves little or no thermal margin at the stated 150°C continuous condition and should not be selected without supplier-specific long-term thermal-age data and a defined derating policy.
PBT is appropriate for conventional 2.54 mm through-hole headers because of its cost and dimensional stability, but its stated HDT is 205°C and it is not an SMT-reflow material [S5]. More importantly, its 120–130°C continuous-use indication is below 150°C [S1]. The mainstream low-cost PBT choice is therefore wrong for this duty unless the actual continuous temperature and duration are lower than assumed.
Check Molding, Reflow, and Assembly Conditions
SMT assembly requires a 260°C peak if lead-free reflow is used, with the identified process window extending to 240–260°C [S2][S5]. A housing limited to 150°C in service still requires separate reflow capability; HDT is not a substitute for a resin-specific reflow classification.
That mechanism explains blistering, delamination, and microcracking. Low-moisture PA9T, PPS, or LCP reduces this risk, while drying procedures and moisture-barrier grades can also control it [S2][S5].
Processing temperature also affects tooling and cycle time. PPS and PEEK may add 20–35% to mold-steel requirements because their processing temperatures exceed 300°C [S1]. Confirm nozzle, mold, purge, and shear limits from the exact resin grade rather than from the polymer-family name. Do not substitute a nominally equivalent resin without rerunning cure, shrinkage, weld-line, moisture, and terminal-force trials [S3][S5].
Validate Electrical, Flame, and Mechanical Requirements
The material choice must satisfy more than heat: dielectric strength, insulation resistance, tracking resistance, arc behavior, chemical resistance, latch fatigue, and flame performance all affect connector reliability [S3]. PC and PC/ABS blends are associated with UL 94 V-0 options in the selection matrix, while PPS is also listed as V-0; the final grade and thickness determine the certification, not the family label alone [S1].
Terminal retention depends on long-term creep and relaxation, so define an allowable contact-normal-force loss over the service life rather than relying on room-temperature pull-force results. Validate retention at 150°C, after thermal aging, after humidity conditioning, and after the applicable reflow cycles. Connector engineering guidance specifically identifies terminal normal force against polymer relaxation as the life-limiting interaction [S3].
Use the qualification plan to separate 150°C continuous exposure from 200°C peaks and 260°C reflow. Track housing mass, key dimensions, latch force, terminal normal force, insulation resistance, and visual cracking after each test interval. These measurable signals expose creep and thermal-aging drift before a production failure.
Apply the Final Material Shortlist
Specify PPS for a conventional 150°C connector housing when creep, chemical resistance, and dimensional stability are primary, and specify LCP when thin walls, low warpage, and SMT reflow dominate [S5]. Consider PA9T when toughness and moisture control outweigh low warpage, but reject standard PA66 and PBT unless supplier data demonstrates an acceptable margin above the actual 150°C continuous profile [S1][S2][S5].
Require the supplier to identify the exact resin grade, continuous-use temperature basis, HDT test condition, moisture absorption, processing window, flame rating, and qualification data. For a production release, verify molded-housing retention at 150°C after thermal aging and reflow, not merely the resin’s nominal temperature rating.