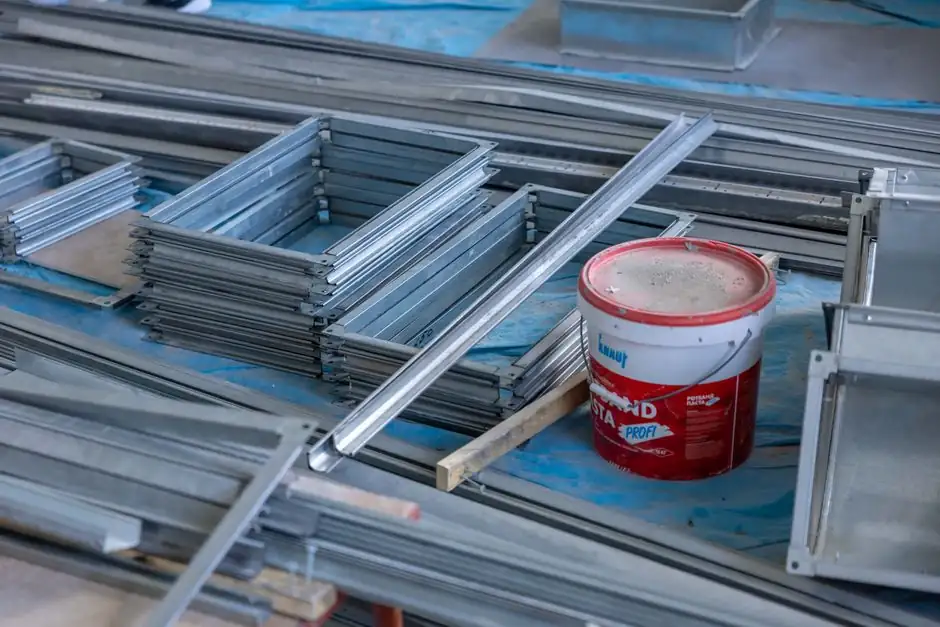
External form vibrators clamped to steel wall panels should be spaced at 3 to 6 foot centers along the formwork run, with 6 foot (1.83 m) centers the most common precast recommendation for rotary units [S1][S3][S5]. The spacing rule derives from each vibrator's radius of action, which Martin Engineering sets at roughly 3 feet (0.9 m) in all directions for rotary external form vibrators, giving the standard 6 foot on-center pattern [S3].
This article covers the spacing math, the difference between internal and external vibration, edge-clearance rules on steel forms, and the operating parameters that determine whether a wall pour consolidates cleanly or comes out of the form with bug holes and lift lines. The principles apply to both site-cast wall pours and precast wall panels built on rigid steel formwork beds.
Spacing Rules: 6 Foot Centers for Rotary External Units
Rotary external form vibrators on steel formwork have a radius of influence of approximately 3 feet (0.9 m) in every direction, so the on-center spacing between clamped units should not exceed roughly 6 feet (1.83 m) for full overlap of the affected zone [S3]. For larger pours, Bison Machinery's field guide to formwork vibration also lands on the 6 foot number for external vibrators on precast forms [S5]. The Deca Vibrator guide corroborates the 3 to 6 foot (0.9 to 1.8 m) window as a good working range when clamping vibrators to formwork [S1].
For internal (immersion) vibrators the math shifts, because the radius of action is governed by the poker head diameter: the radius of influence is about 4 times the head diameter, and insertions should be spaced at roughly 1 to 1.5 times that radius, with a target overlap of one third of the radius to avoid untreated zones [S5]. NBAce Tools frames the same rule as 1.5 times the visible radius of action per insertion, with the poker inserted vertically and the previous lift penetrated by 2 to 4 inches (50 to 100 mm) [S2].
Internal vs External Vibration on Steel Wall Forms
External vibration is the right choice for thin or heavily reinforced wall sections where an immersion poker cannot fit between the rebar mat and the form face, and for precast wall panels cast on rigid steel forms [S2]. Internal vibration is the default for most walls, columns, beams, and slabs because the poker delivers energy directly into the lift; for wall pours, the head frequency typically runs 8,000 to 12,000 vibrations per minute, enough to liquefy the mix temporarily without segregating the aggregate [S2].
Steel formwork is a good partner for external vibration because the panel mass and stiffness transmit the rotary force efficiently into the concrete; for that reason, Martin Engineering recommends permanently mounting rotary external form vibrators to steel forms, since permanent brackets give more predictable energy transfer and a longer vibrator life than portable clamping with frequent handling [S3]. The same source notes that electric rotary units are quieter and cheaper to run than compressed-air units, while compressed-air units are preferred in damp conditions where electrical shock risk is harder to control [S3].
Edge Clearance, Hold Time, and Insertion Depth
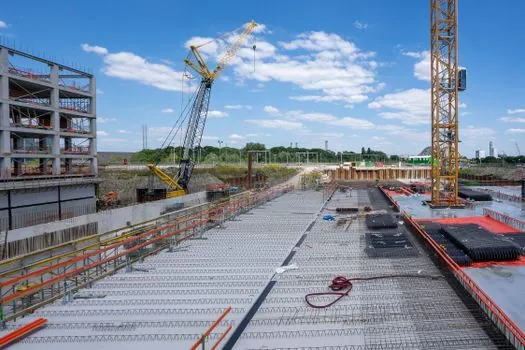
On steel wall forms, keep the immersion vibrator head 7 to 10 cm (roughly 3 to 4 inches) away from the form face to avoid damaging the form liner and to prevent the steel panel from absorbing energy that should be going into the concrete [S5]. Insertions should be made in a regular pattern, either a square grid with one third of the radius of influence overlapping between adjacent insertions, or an offset zigzag pattern that uses the same overlap principle but spaces the heads in a staggered layout for better coverage in heavily reinforced sections [S5].
Hold each insertion 5 to 15 seconds for internal vibration, withdrawing slowly at about 2.5 to 7.5 cm/s, with the lower end of that range usually producing the best surface finish [S2][S5]. On external form vibrators, Martin Engineering's rule of thumb is to run the vibrator for roughly 1 to 2 seconds per 1 to 2 inches of form height; a 4 foot (1.2 m) high wall form therefore needs about 48 to 96 seconds of vibration, applied during the filling process so entrapped air can move upward and escape before the form is fully topped off [S3].
Consolidation Stages and What the Operator Should See
Internal vibration has two visible stages, leveling and de-aeration; in the leveling stage, the rapid oscillatory motion temporarily liquefies the mix, coarse aggregate becomes suspended, voids between aggregate fill with mortar, and the concrete settles into corners and around rebar [S4]. In the de-aeration stage, remaining entrapped air bubbles rise to the surface and escape, with the largest bubbles leaving first, and vibration should continue until large bubbles stop breaking the surface, the coarse aggregate is fully embedded, and a thin film of mortar appears on top and along the form faces [S4].
For external wall vibration, the equivalent end-point indicators are the same: concrete levels off in the form, coarse aggregate becomes embedded, a thin film of mortar forms on the top surface, and air bubbles stop percolating [S3]. The pitch of the vibrator is also a usable signal: when the poker is first inserted, frequency drops, then climbs, then becomes constant once the mix around the head is largely free of entrapped air [S4]. Operators who stop at the leveling stage and skip de-aeration are the most common source of bug holes and lift lines on finished wall surfaces [S4].
Mix, Power, and Practical Comparison of Methods
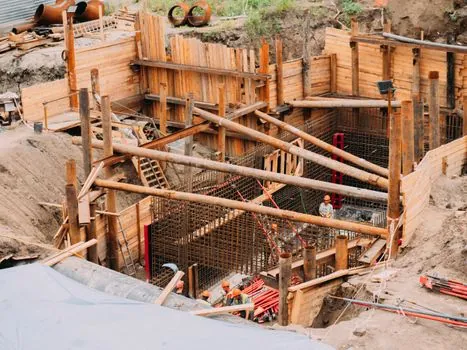
Mix stiffness drives the choice of vibrator. Stiff, low-slump concrete responds better to slower-speed rotary force at higher amplitude, while higher-slump, pumpable mixes consolidate well with higher-frequency rotary force [S3]. For the same wall, the three main method options compare as follows:
Internal (immersion) vibration: highest energy density at the head, best for standard wall thickness with rebar spacing that admits the poker; spacing rule 1 to 1.5 times the radius of action, roughly 4 times head diameter; operator must penetrate the previous lift by 2 to 4 inches [S2][S5]. External (form-mounted) vibration: required for thin or heavily reinforced walls and for precast on steel forms; spacing rule 6 foot on-center for rotary units; permanent mounting on steel panels preferred for predictable energy transfer [S3][S5]. Surface (screed) vibration: limited to slab depths of about 6 inches (150 mm) or less, not applicable to wall formwork [S5]. The general-purpose handheld concrete vibrator in use across most wall pours today operates in the 8,000 to 12,000 vpm range, with head diameters from roughly 25 mm to 75 mm matched to rebar spacing [S2].
Common Failure Modes and What the Spacing Prevents
Spacings that exceed 1.5 times the radius of action leave untreated zones where honeycombing, weak rebar bond, and surface voids are likely, while over-vibration at any single insertion can drive aggregate segregation and mortar loss at the form face [S2][S4]. Untrained operators who only level the concrete and skip the de-aeration stage are the most common cause of bug holes and lift lines on exposed wall surfaces [S4]. The same entrapped air, up to 20 percent by volume in freshly placed concrete, is what proper spacing and hold time are designed to remove [S4].
On the concrete vibrator side, the working envelope is well defined: 5 to 15 second insertions on a 1 to 1.5 times radius grid for internal units, 6 foot on-center spacing for external units clamped to steel formwork, 7 to 10 cm edge clearance to the form face, and 48 to 96 seconds of external vibration for a 4 foot tall wall [S2][S3][S5]. For precast producers running wall panels on climbing formwork or on steel diaphragm wall beds, the same rotary external spacing rule applies because the form stiffness and mass are similar; portable clamping is acceptable for short runs but permanent brackets remain the longer-life choice [S3][S6].
Track these signals on the next wall pour: measure the actual radius of action on site by watching how far air bubbles escape from the poker head, not from a catalog number, and check that the 6 foot on-center external spacing produces visible mortar film along the full length of the form within the prescribed run time [S5]. If the gap between adjacent external units exceeds 6 feet or the form face shows dry pockets after the pour, the spacing is the first variable to tighten before any change to mix or vibrator size.
See also our earlier report, Skylight Curb Cladding Materials: Wood, Aluminum, PVC, Steel.