
14-Inch vs 16-Inch Cut-Off Saw Capacity Guide
A 16-inch abrasive saw offers greater cutting depth and heavier-section capacity, while a 14-inch saw reduces cost, weight, and kerf for routine steel work.
Read →Industry News · Category
A 16-inch abrasive saw offers greater cutting depth and heavier-section capacity, while a 14-inch saw reduces cost, weight, and kerf for routine steel work.
Read →
Choose a bench-mounted cut-off machine for fixed, repeatable work; choose a portable stand for site access, with stability and wheel compatibility decisive.
Cut-off wheel arbor compatibility depends on the machine spindle, wheel bore, backing flanges, and approvals, not the wheel brand. Match diameter, bore, thickness, speed, and guard.
Choose a diamond blade for repeated concrete, brick, block, stone, tile, or asphalt cuts; use an abrasive wheel for metal and thin stock.
For stainless steel cut-off wheels, select a resin-bonded abrasive wheel with a stainless-steel-compatible grain, such as ceramic alumina, in Type 1 or Type 27 geometry.
Cuplock uses a four-way cup-and-blade joint at 500 mm intervals; Ringlock uses an eight-way rosette-and-wedge joint for more flexible geometry.
Frame scaffolding usually erects faster for small, low-level access towers, while Cuplock gains productivity on repetitive, tall, straight-run structures with greater load capacity.
Choose CD for 1–10 mm studs on thin sheet and DA for 3–25 mm studs needing deeper welds. Compare ferrules, cycle time, power, and labor.
A handheld marble cutter can fit a $15-$35 blade, but granite cost depends on cut length, thickness, blade wear, edge finish, and labor rather than one universal rate.
Hydraulic self-climbing formwork costs more initially, but lower crane use and shorter cycles can reduce cost per floor when reused across many lifts.
A cordless rebar bender’s bends per charge depend on battery capacity, bar diameter, bend count, steel grade, and ambient conditions, not a fixed universal figure.
Use a continuous-rim diamond blade, run wet, for porcelain tile cuts that need a clean edge and low chipping; choose segmented only for rough masonry cuts.
Concrete vibrators rent for $45–$110 per day. Compare that rate with ownership cost divided by annual use days before buying.

The LPS10/80 wet shotcrete pump has an adjustable output of 5–10 m³/h and an output pressure of 80 bar, while REED concrete pumps have concrete pressures from 69 to 145 bar.
Choose a walk-behind concrete saw for deep, long highway cuts; use a truck-mounted saw body when transport, fuel, water, and secure storage justify the setup.
Choose a scarifier for aggressive removal, deep traction grooves, and slab leveling; choose a grinder for shallow coating removal, controlled texture, and a smoother finish.
Select a concrete groove cutter with a declared A(8) below 2.5 m/s², sharp diamond blades, and maintenance controls that limit vibration.
Choose a single-blade cutter for narrow, controlled grooves; choose a multi-blade gang saw for parallel cuts and high production in qualified stone applications.
A highway concrete groove cutter’s work-zone noise rating must be model-specific and measured at a defined distance; the research supplies no universal dBA label.

Concrete groove cutters typically cut 40–65 mm with angle grinders, 100–125 mm with cut-off saws, and 150–450 mm with walk-behind saws per pass.
For continuous concrete groove cutting, select a 13.5–15 hp motor, matched to blade speed, depth, aggregate, and duty-cycle limits.
Use a diamond blade for concrete groove cutting; carbide is less suitable for abrasive concrete.
Concrete pavement grooving commonly targets depths of 3.2–6.4 mm, with depth control and free-floating heads required to maintain uniform cuts.
Concrete groove cutter cost rises with blade count, cutting width, engine power, and water system; listed machines span Rs 48,300 to Rs 1,05,800.
Standard rumble-strip grooves typically use 12-inch spacing, with groove widths of 5–7 inches and a depth near 0.5 inch. Select the agency pattern, pavement type, and blade setup before ordering.
For hard concrete aggregate, select a soft-bond diamond groove cutter segment so the metal matrix wears faster and exposes fresh cutting diamonds.
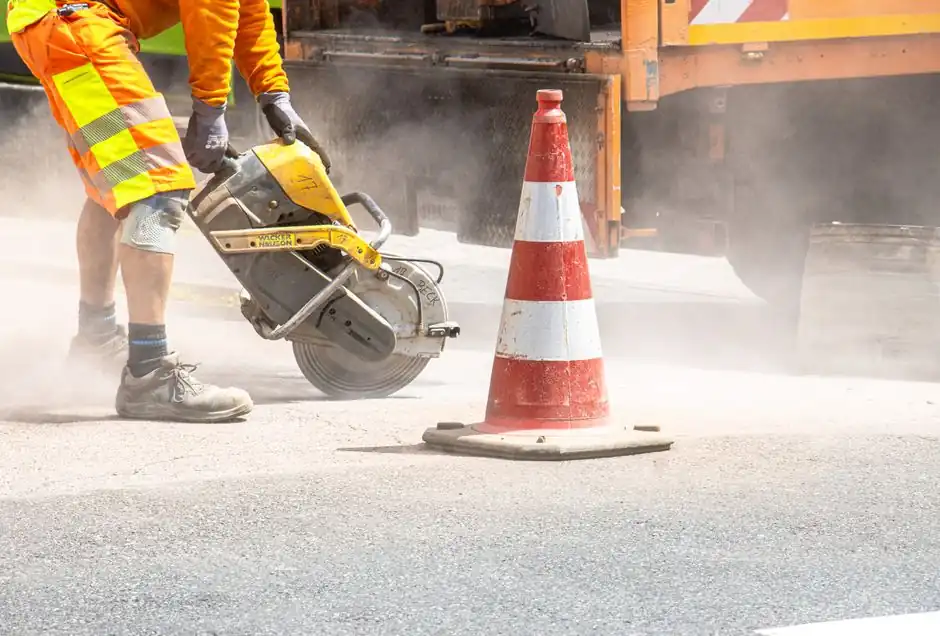
A concrete groove cutter blade for cured concrete must match the saw’s RPM, diameter, bond, and arbor; a 14-inch blade is commonly rated near 2,592–4,365 RPM.
Concrete groove cutter blades typically require 2–5 L/min of continuous water from handheld saws, while walk-behind and wall saws commonly need 10–30 L/min.
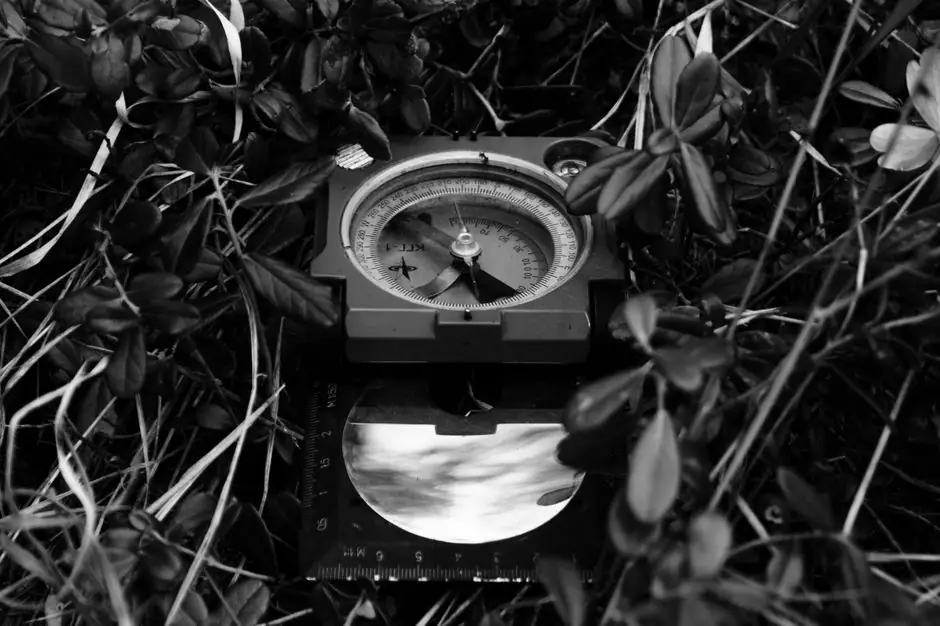
Use a compass theodolite when bearings must reference magnetic north without powered electronics; use an electronic theodolite for repeatable angle work and digital data capture.
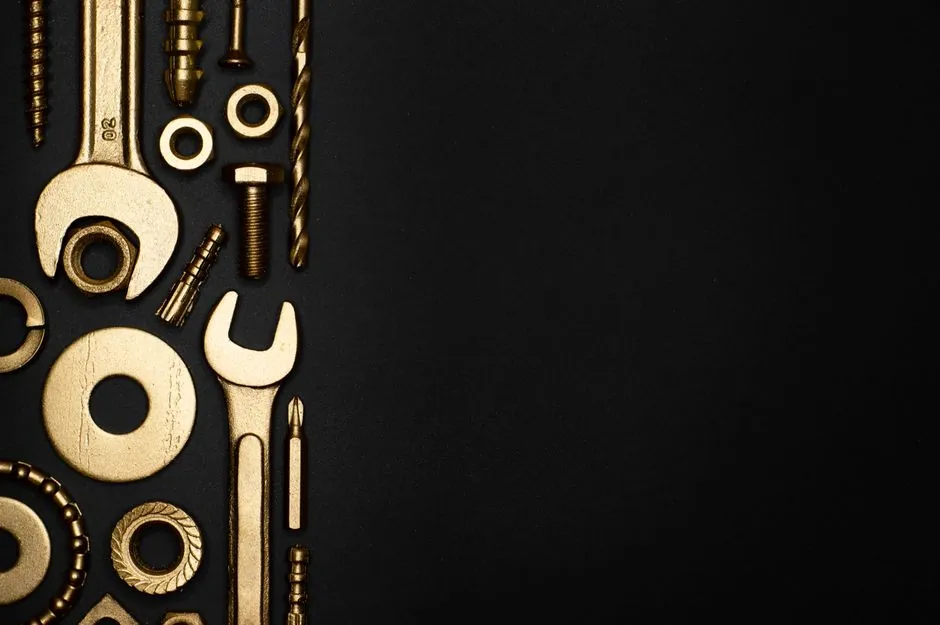
Choose an open-end wrench for restricted clearance, a combination wrench for mixed access and torque, or an offset box wrench for confined high-torque work.
Cold chisels suit general metal cutting; cape chisels cut clean grooves, while diamond-point chisels form V-shaped grooves and prepare weld prep.
Coil rebar and straight bar use the same mill gate price, but coil usually lowers handling, cutting, and replacement cost per delivered ton.
CNC plasma gives repeatable, automated sheet-metal cuts, while handheld plasma wins for portable repair work. Choose by volume, geometry, thickness and edge requirements.
Choose CNC machining for repeatable, programmed production, or manual milling for operator-controlled one-off setups.
A climbing bolt is not assigned a safe working load from diameter alone. Size the 25 kN-rated hardware, base material, installation, load direction, and rope-system forces together.
Climbing formwork weight per square metre must be calculated from the complete assembly, not the panel alone, because bracket load and platform mass dominate.
Choose climbing formwork for rising concrete work and suspended platforms for facade finishing; match access method to structure, logistics, loads, and controls.
Choose self-climbing formwork for repetitive high-rise cores with hydraulic climbing, and scaffold for irregular geometry, short access needs, and lower initial cost.

Climbing formwork tie spacing must be reduced for high-pour-rate concrete. Typical snap ties start near 610 mm vertically and 914 mm horizontally, then tighten from pressure calculations.
A climbing formwork system’s wind rating is configuration-specific: published limits range from 72 km/h working wind to a tested 208 km/h, depending on system and load case.
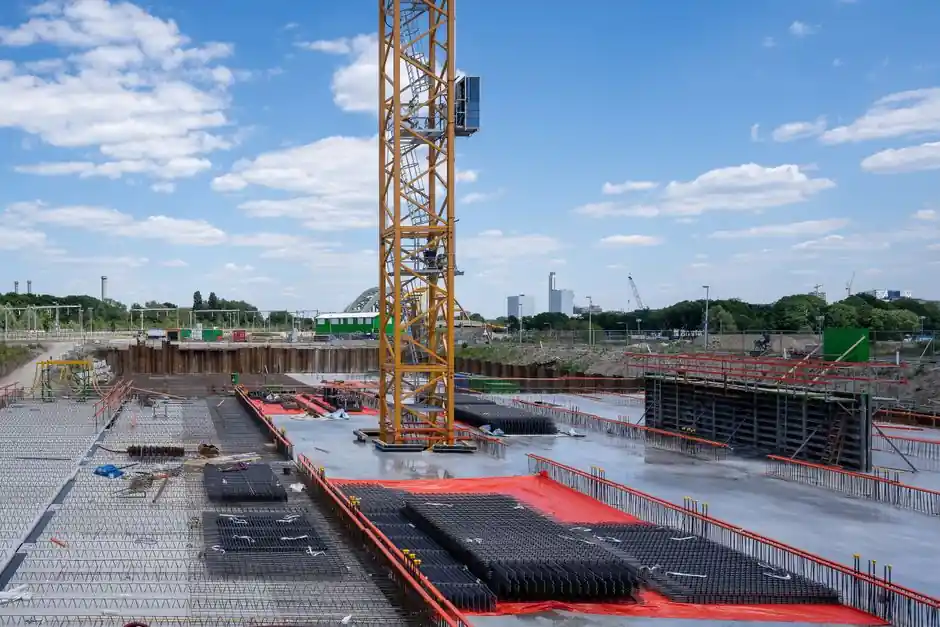
KLK 230 can be used to build a 2.30 m wide working platform with no formwork on the platform, while CB 160 is a climbing-formwork system whose published excerpt refers to cutting handrail boards to match the platform width.
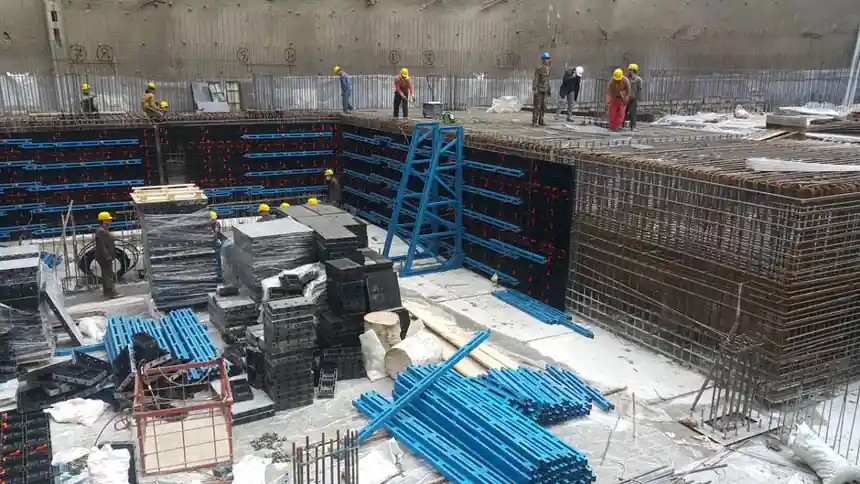
Climbing formwork platform capacity includes 1.50 kN/m² per KLK 230 level and 400 kg/m² for one hydraulic top platform, while Hünnebeck bracket systems can carry up to 150 kN.

Climbing formwork platforms generally need edge protection from an exposed fall height of 6 ft, with guardrails at least 42 in high under OSHA.
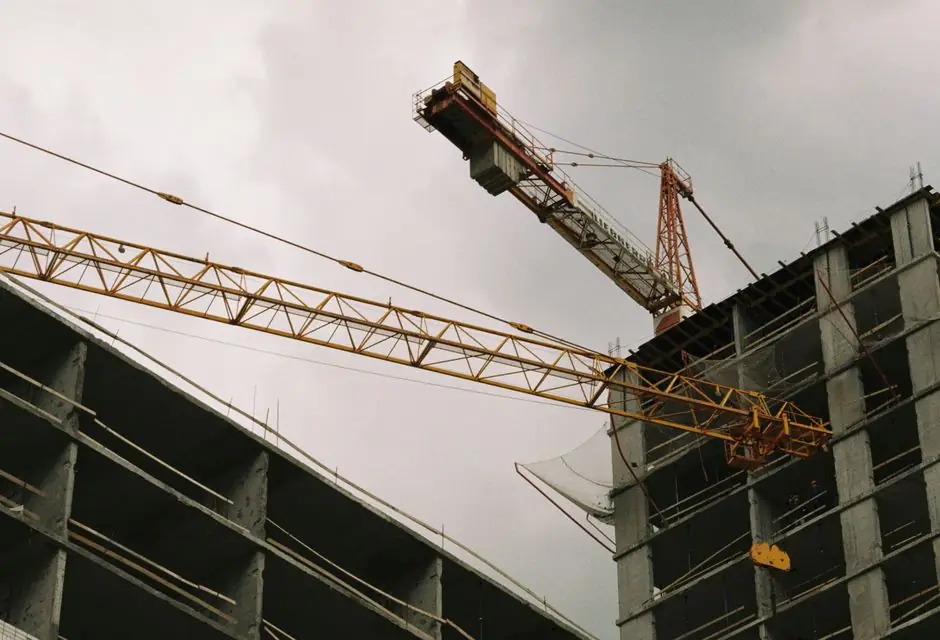
Climbing formwork bracket spans range from 2.30–4.75 m in documented systems, but allowable spacing depends on loads, wind and anchoring.
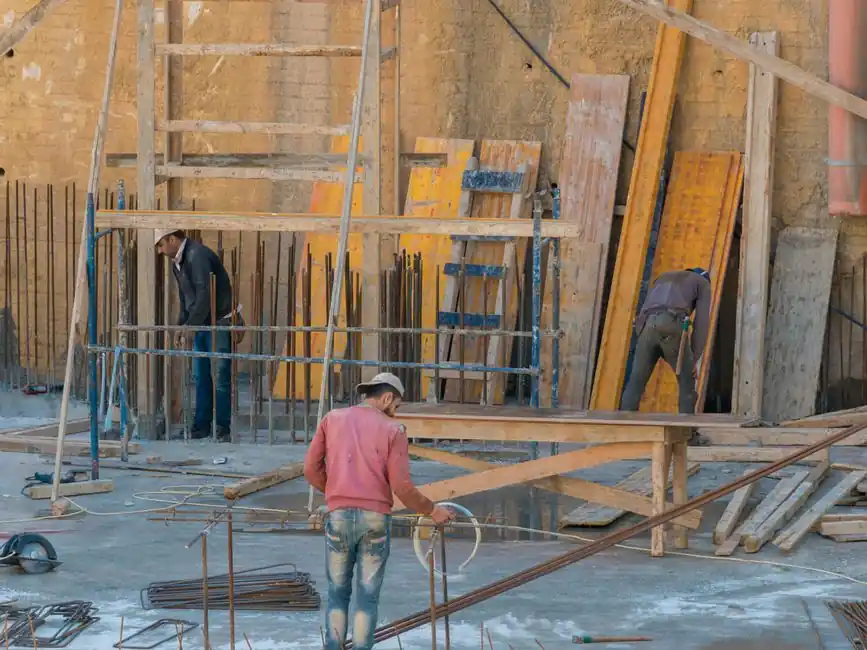
Choose steel for repeated pours and rigid walls; choose plywood for complex geometry, lower initial cost, and limited crane access.
A two-crew, eight-person jumpform team can complete one floor cycle in 5.74 days, but crew size, concrete strength, geometry, and sequencing determine the actual cycle.

For a 300 mm core wall, bracket spacing is set by the formwork design, load path, wall ties and wind load, not by the 300 mm wall thickness alone.

Choose an internal stair tower for frequent climbing above 5 m; use a ladder only for constrained, temporary access where space and cost dominate.
Plan rebar splices with a 750 mm offset or 1.5 db clear gap, using coupler diameter, concrete cover, and placement access as controls.

Worm-drive saws deliver higher torque for heavy cuts, while sidewinders run faster at lower weight for sheet goods and general carpentry.
A 4×8 ft sheet of ¾ in plywood weighs over 80 lb, so a circular saw with a straight-edge guide is safer for solo breakdown than a table saw.

Circular saw vibration is best controlled at the blade and workholding system, with thin 1.5 mm blades, 40–50 teeth, 80–120 dB(A) noise, and resonance avoidance as key criteria.

A track saw provides more repeatable straight cuts than a freehand circular saw, while a guided circular saw offers lower cost and greater portability for common woodworking.

Choose aluminum for a stiffer, lighter shoe; choose stamped steel for impact resistance and low cost, but verify flatness before precision cuts.

A riving knife usually offers better kickback prevention than a fixed splitter because it stays close to the blade and rises with it, but neither device prevents all kickback.
Circular saw noise for indoor framing can span 80–120 dB(A). Select low-noise blades, control vibration, and verify the saw’s rated output before use.
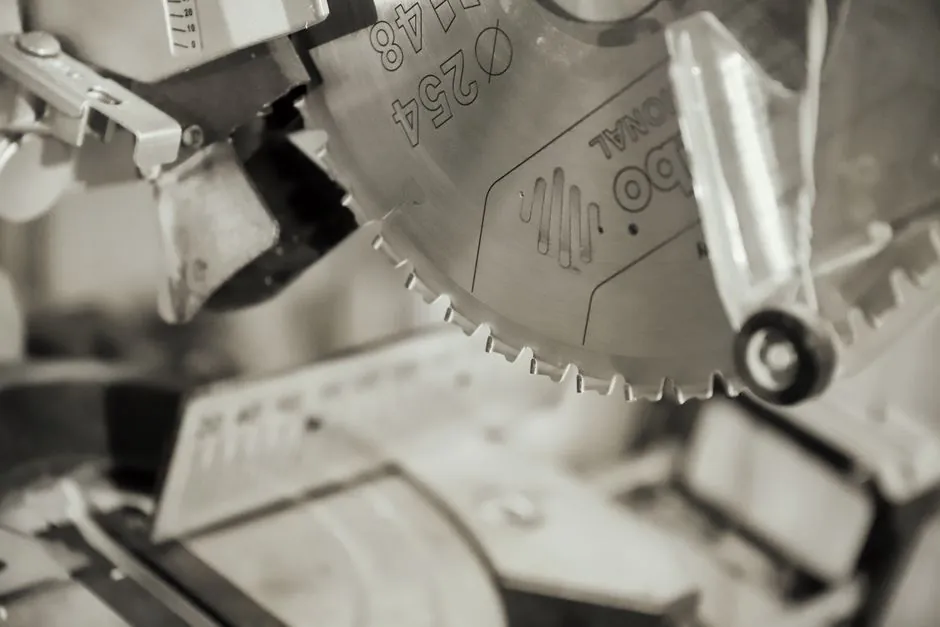
For continuous framing, choose a corded circular saw rated at 15 A for common work, or a 10 1/4-inch model rated at 14 A for larger capacity.
SDS-Plus suits anchor holes to about 30 mm in concrete; SDS-Max takes over for larger holes and sustained chisel demolition. The shank standard, impact energy and duty cycle decide before brand does.
A left-blade circular saw gives right-handed users a clearer cut line, but sightline alone does not determine safety, balance, or blade compatibility.
For most circular-saw crosscuts, a calibrated base-plate notch is more dependable than a laser guide; lasers help only when the line is visible and accurately aligned.
A healthy electric-brake circular saw should stop within about 2–3 seconds of trigger release; longer coasting indicates degradation or failure.
A 7-1/4-inch circular saw cuts about 2-5/8 inches at 90 degrees, but beveled depth falls as the blade tilts. Set the saw to the complementary angle when the cut exceeds 45 degrees.
Choose by cut depth, material density, and blade geometry: 7¼-inch saws suit thick lumber, while LVL and PSL need more capacity than solid wood.
Brushless motor technology and power delivery are the main cost drivers in a circular saw, while corded-brushed models can offer the lowest purchase price.
Cordless circular saws can support continuous cutting, but runtime depends on battery capacity, load, and pack rotation. Corded saws remain better for unrestricted heavy-duty production.
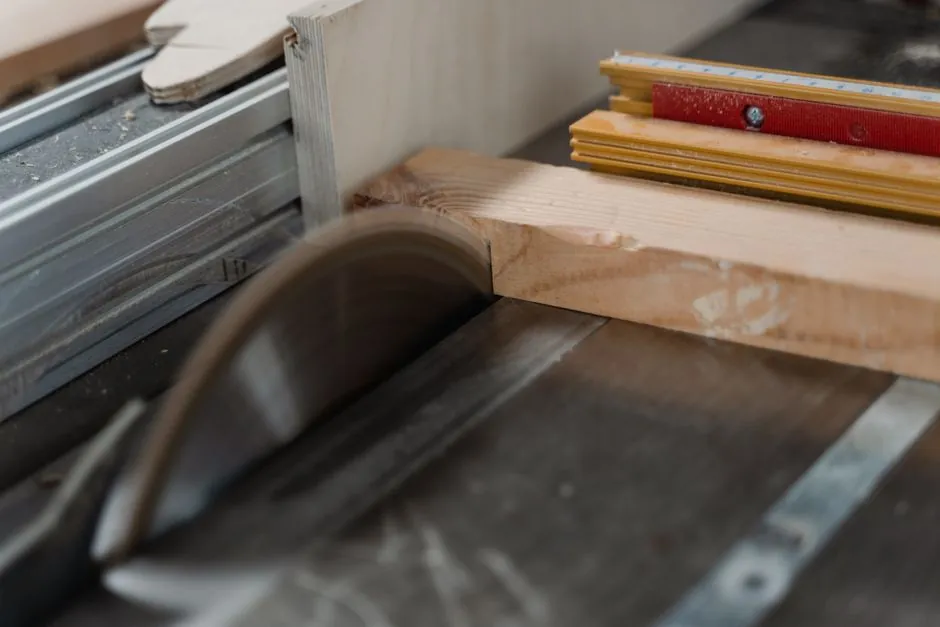
Choose FTG carbide teeth for fast ripping with strong chip clearance, and ATB teeth for clean crosscuts with less splintering. The correct grind follows the cut direction.
A brushless circular saw can run 25–50% longer than a brushed model on the same battery, with better efficiency and lower wear.
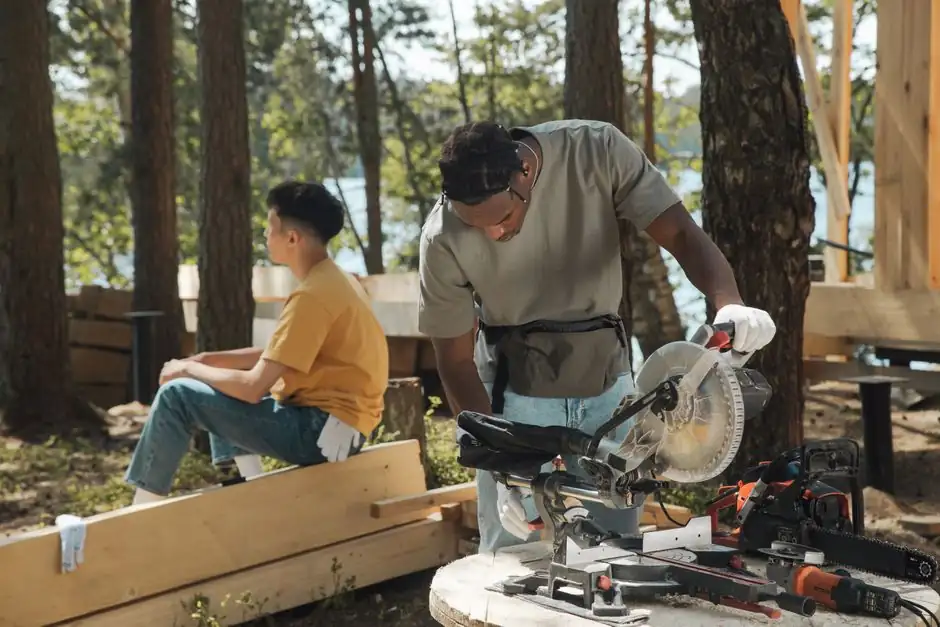
Use 24T–40T for fast wood ripping, 40T–80T for finish work, and 60T or more for aluminium and metal, matching tooth geometry to the material.
Use a dedicated carbide-tipped acrylic blade with a negative hook angle to reduce chip-welding, melting, chipping, and cracking in cut acrylic sheet.
A 7-1/4-inch blade typically cuts 2-1/2 to 2-3/8 inches deep, while an 8-1/4-inch blade offers about 2-3/4 to 3 inches.
A 5/8-inch arbor specifies the blade center hole, while a diamond knockout is a removable adapter. Verify both before mounting a circular saw blade.
Circular saw bevel adjustment commonly spans 0–45° or 0–50°; verify the model scale, square the base, and test-cut before production.
Choose 18V for portability and platform consolidation; choose 36V for sustained cutting power, larger capacity, or corded operation.
A 16-5/16-inch saw cuts 6x timber in one pass, while a 10-1/4-inch saw usually needs two passes for oversized timbers.
Climbing formwork can be reused across tower projects, but only after verifying geometry, lifting method, anchor compatibility, condition, and planned cycle count.
A hand-held power mixer cannot reliably mix concrete with coarse aggregate; use a rotating-drum or paddle mixer sized for the 40 mm aggregate limit.
A cordless drill can mix small batches of thin-set mortar, but only with a mortar-rated drill, paddle and controlled speed. For larger batches, use a power mixer.
Choose a 25-tooth SDS-Max bushing bit, 40 x 300 mm, for controlled concrete roughening in a demolition hammer. Match the shank exactly before purchase.
Choose an integral motor spindle for high-speed finishing, a belt spindle for economical low-speed torque, and a geared spindle for low-speed heavy cutting.
BS 2482 timber scaffold boards offer low-cost, light handling, but steel planks better suit harsh sites, high traffic, corrosion, and long reuse cycles.
Brushless motors reduce brush and heat failures in high-duty concrete vibrators, while universal motors remain simpler and less expensive for intermittent work.
Bluetooth laser distance meters typically cost $60–$199 versus $20–$69 for basic models, but connectivity adds value only for recurring digital workflows.
Choose 3×21 for control and 4×24 for stock removal; their belts are not interchangeable.
Direct-drive walk-behind power trowels deliver lower center of gravity, less wobble, and no belt maintenance versus conventional belt-drive units, at a 2025 retail price of $3,250-$4,295 for Arrow Master F30-F46 models with Honda GXV engines.
Cordless concrete vibrators on 18-22V Li-ion platforms typically deliver 40 minutes to 1 hour of active run time per charge, with 4000 mAh packs rated near 1 hour and 5.0 Ah packs driving 12,500-15,000 VPM brushless heads over a 4 ft shaft. Real output tracks head diameter, slump, and concrete press
Ball-end hex keys can typically engage a socket cap screw at up to a 25° off-axis angle, but their smaller contact patch caps torque delivery well below a straight hex key, so high-torque or break-out jobs belong on a straight-end tool.
Automatic electroslag pressure welders deliver 1.5 to 3.0 kW of regulated heat input with closed-loop wire feed and slag-pool monitoring, beating manual units on deposition rate, repeatability, and weld defect rates per ESAB guidance. Choose automatic for vertical column splices above 25 mm thi
Resin fiber disc performance on an angle grinder is set by the backing pad: ribbed/firm rubber for 24-40 grit stock removal, smooth/medium for 50-80 grit blending, and flexible/hard pads for 100+ grit finishing. Match the pad to the disc grit, spindle thread, and rated RPM.
An automatic stud feeder cuts per-stud cycle time from 8 to 15 seconds manually down to 1 to 2 seconds on a CNC cell, a 6x to 15x throughput gain, and one capacitor-discharge feeder variant tops out at 60 studs per minute.
For wet job sites, an IP65 minimum is the practical baseline for an automatic level, with IP66/67 specified where hose-down, submersion, or heavy rain is routine. Pair the housing rating with sealed eyepieces, nitrogen-purged optics, and a compensated pendulum to keep the compensator alive.
For a one-shot benchmark transfer under 100 m on an open, calm site, an automatic level delivers 1-2 mm height-only accuracy with a 2-person rod-and-instrument crew, while a total station adds horizontal coordinates at 2-5 mm entry-level or 1-2 mm professional distance accuracy but trades 1.5-3x the
For indoor drop-ceiling grid leveling, a self-leveling line laser with a 360° horizontal plane beats a manual automatic (optical) level on speed, one-person workflow, and continuous reference. Optical automatic levels still win on long sightlines and outdoor accuracy over 30 m, but they are the wron
Automatic levels use a gravity-suspended compensator to self-level after coarse setup, while dumpy levels require manual bubble centring via three foot screws. Fixed-focus optics suit short-range crew work; adjustable-focus telescopes extend sighting distance and stadia accuracy on longer runs.
The 5/8"-11 UNC thread is the de facto standard for survey and construction laser tripods, with rotary, line, and point laser mounts, plus laser distance meters and total stations, all mating to this coarse thread pattern.
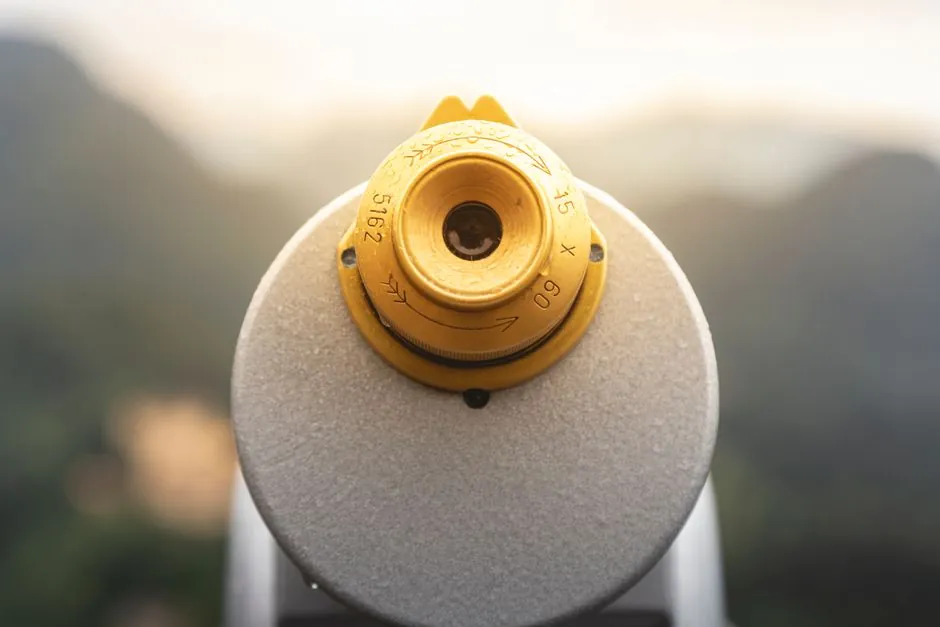
Surveyor's automatic levels typically ship with 20x, 24x, 28x, or 32x telescopes; 28x and 32x are the practical ceiling for long sightlines because beam stability and compensator range degrade above ~35x. For runs beyond 90 m, pick 28x or 32x with a 36 mm objective and a magnetic compensator.
Automatic level standard error per double-run kilometer is published as a 1-sigma figure, typically ±0.5 to ±2.5 mm/km depending on class, with ±1.5 mm/km the common mid-range for general engineering work and ±1.0 mm/km required for second-order precise leveling per kilometer-of-height-difference li
Precise leveling staff graduations are spaced at 0.5 mm intervals on dual invar columns for first-order work, while everyday E-pattern staffs use 10 mm blocks with 1 mm or 5 mm subdivisions, and accuracy spans from about ±0.3 mm/m to ±1.5 mm full length. Match the graduation increment to your instru
Anti-reflective (AR) coatings cut lens surface reflection from roughly 8-10% to under 1%, boosting light transmission above 98% and delivering measurably sharper, lower-glare vision across driving, screen, and clinical tasks.
Automatic level operating temperature is typically specified as -20 to +50 °C by survey OEMs, though several current catalogs list a derated -10 to +50 °C window. Cold-side tolerance is set by compensator suspension fluid and LCD chemistry; hot-side tolerance is set by seal ageing and battery chemis
Automatic level minimum focusing distance has tightened to 20 cm (7.9 in) on the Topcon AT-B series, versus 50 cm and 1 m on prior generations, with Nikon AP-8/AC-2S/AX-2S and AE-7 specs landing at 0.75 m (2.46 ft) and 0.98 ft respectively. Shorter minimum focus enables work in confined spaces and o
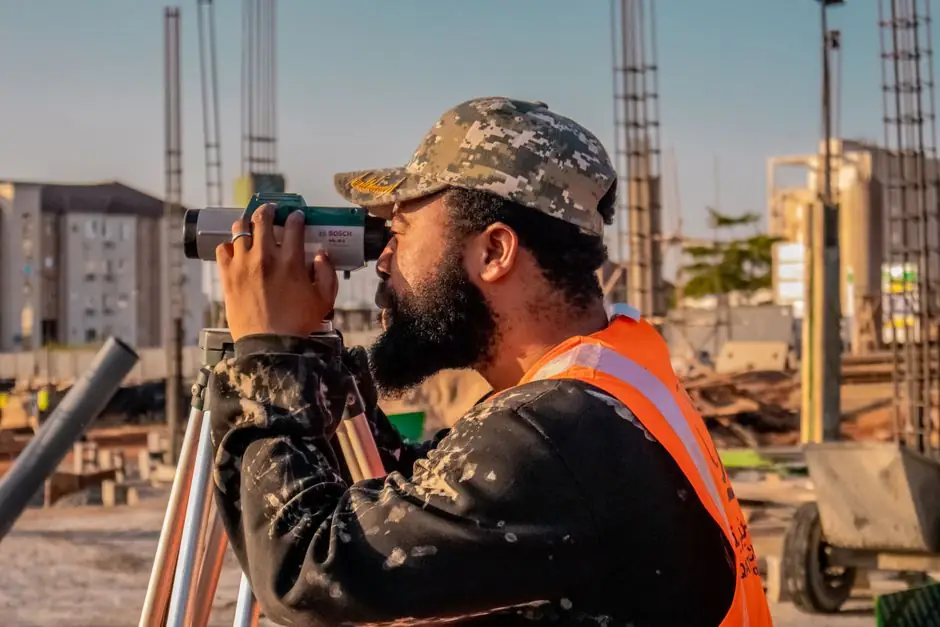
Automatic level horizontal circles ship in two graduations: 360-degree (sexagesimal, 1° increments) for general North American layout work, and 400-gon (decimal, 0.5–1 gon increments) for metric European cadastral jobs. Pick 360° for imperial specs and 1° accuracy; pick 400 gon for metric work where
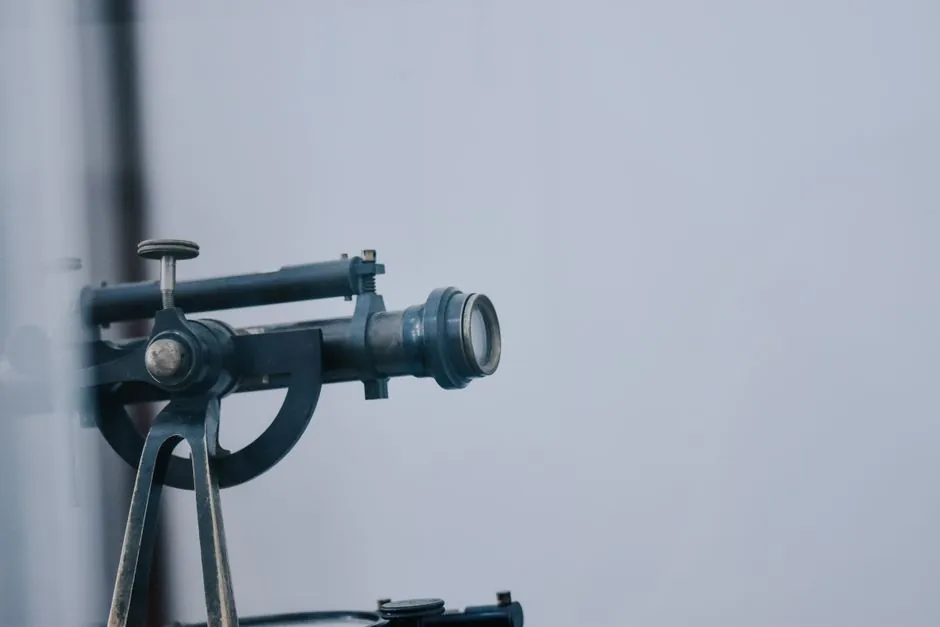
An automatic level with an erect-image telescope presents a vertically and laterally corrected view through extra erecting optics, while an inverted-image (standard) telescope shows a view that is upside down. For surveying work, erect-image optics reduce field-operator disorientation on terrestrial
Automatic level pricing is driven primarily by optical quality (magnification 20x-32x, glass vs polymer objectives) and compensator precision (≤0.5 mm self-leveling accuracy, ±15 min working range), with ISO 17123 conformance and IP-rated housings as secondary cost multipliers. Mid-range instruments
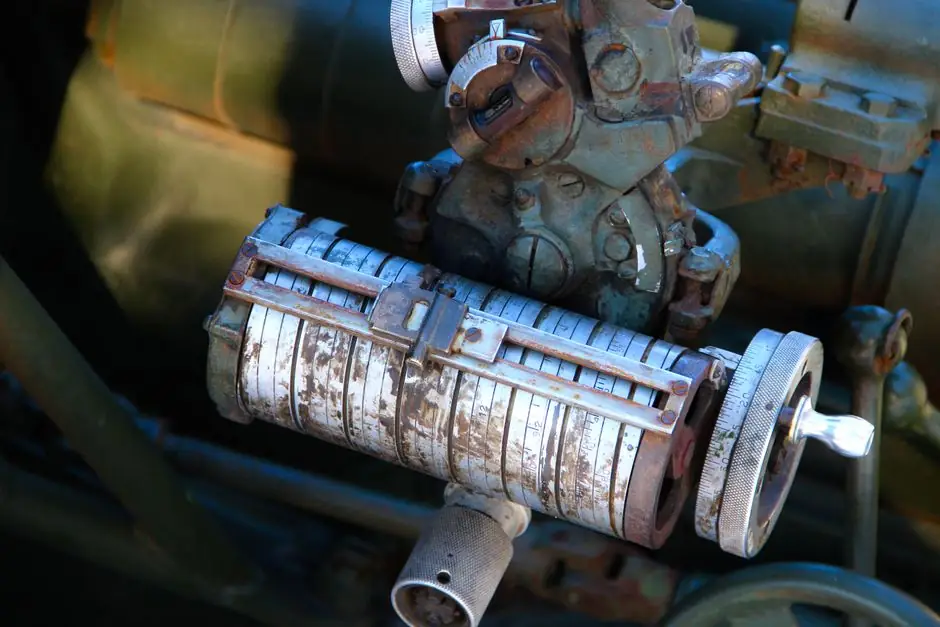
Magnetic and air-damped compensators both gravity-hang the optical prism inside an automatic level, but they dissipate swing energy through different physics. Choose magnetic for vibration-heavy sites; choose air when local electromagnetic fields threaten eddy-current dampers.
An autocollimation theodolite delivers sub-arcsecond squareness checks on machine axes by reflecting a collimated reticle image back through the telescope; selection hinges on reticle resolution, electronic readout tier, and working distance, with one-second optical theodolites remaining the referen
ATEX-rated laser distance meters must combine Ex d flameproof or Ex i intrinsically-safe enclosures with Zone 1 IIC T4 gas-group certification, Class 2 laser output under IEC 60825-1, and an IP65 chassis; 2026 handheld and fixed-mount models span 0.05–500 m range with 1–3 mm typical accuracy for haz
Asphalt cutter blade widths for demolition hammers cluster in 3 in, 4 to 5 in, and 5 to 5-1/2 in bands, matched to 1-1/8 in hex, 1-1/4 in hex, or SDS-Max shanks per current OEM catalogs.
For outdoor sites, IP23 is the minimum ingress protection rating that arc welding power sources should carry, per TWI guidance and OSHA 29 CFR 1910.254 weather-exposure clauses. IP23S units are not waterproof, and damp-site work also demands OCV reduction controls for shock mitigation.
Hook-and-loop (Velcro) and threaded backing pads both mount 4-7 inch polishing pads to an angle grinder spindle, but they answer different workflow needs. Hook-and-loop wins on changeover speed and grit-progression work; threaded pads win on heavy duty, high-RPM, and contamination-tolerant jobs.
Maximum safe cutting-disc thickness on an angle grinder is governed by three coupled limits: spindle no-load RPM, disc diameter, and the EN 12413 maximum surface speed of 80 m/s. For a 125 mm grinder at ~11,000 RPM, optimal cutting discs are 0.8–1.6 mm; 3.0+ mm discs are restricted to stationary mac
For small parts work, a bench-mounted grinder gives better angle repeatability and heat control at 1,750–3,450 rpm, while a handheld angle grinder with a vise or jig trades precision for mobility and disc versatility. Pick bench for tool sharpening and repeat geometry; pick handheld for one-off cuts
OSHA's 29 CFR 1926.1153 Table 1 lets contractors use either a wet water-feed system or a vacuum dust collection system (VDCS) with a commercially available shroud on handheld angle grinders cutting or smoothing concrete; the VDCS path requires at least 25 cfm of airflow per inch of wheel and a HEPA-
Folding aluminum step platform ladders for standing work typically pair a 10–18 in wide top platform with 3–5 in deep treads and a 300–375 lb load rating, folding down to roughly 5–6 in flat thickness for transport and storage. Top step depth is the single most important standing-comfort number; cho
An aluminum podium ladder with a full guardrail is the more stable choice for prolonged standing work, while an aluminum step ladder wins on portability for short, mobile tasks. For most home and jobsite applications, the decision comes down to reach, weight, and whether the user needs both hands fr
Aluminum multi-position ladders rely on locking hinge assemblies to convert between A-frame, stairway, extension, and scaffold-base configurations, with load ratings typically spanning 250 lb (Type II) to 375 lb (Type IA). The hinge design, spring protection, and lock-state indicator are the three s
Fixed-ladder rails in the US must hold rungs to a 16 inch (41 cm) minimum clear width per OSHA 1910.23(b)(4), with 7 inches of wall standoff and 10–14 inch rung spacing. Portable aluminum ladders need only 11.5 inches of rung clear width, which is why fly-section rail stacks on extension ladders com
Pneumatic clay and trench diggers span 21 to 37 lb in the light-to-heavy trenching range, with blow rates of 1,850 to 2,120 bpm at 34 to 42 CFM and 90 PSI. Pair the tool to carrier class (mini under 7 t, midi 7 to 15 t, standard 16 to 30 t) and soil stiffness rather than buying the heaviest unit on
Air-pick cost drivers are dominated by blow energy, air consumption rate, and downstream pressure losses. A 2 psi discharge pressure increase adds 1.6 to 2% energy use, and a 200 HP compressor running 8,000 hours can spend $137,766.57 per year on energy alone.
An air pick typically needs 4-6 CFM at 90 PSI for continuous operation, so a single-tool setup only demands a compressor matching that rating, while running 2-3 tools simultaneously requires summing their peak CFM plus a 25-30% margin to prevent pressure sag. Tank size scales with duty cycle: 6-gall
A continuous-duty air pick needs 30-50 CFM at 90 PSI, with 25-40% safety margin above the rated value to prevent starvation and motor damage.
Air picks and paving breakers break asphalt with 1,250–1,650 BPM percussion at 60–120 mm piston stroke; longer stroke raises per-blow energy but lowers blow rate, so 90 lb class breakers suit thick lifts.
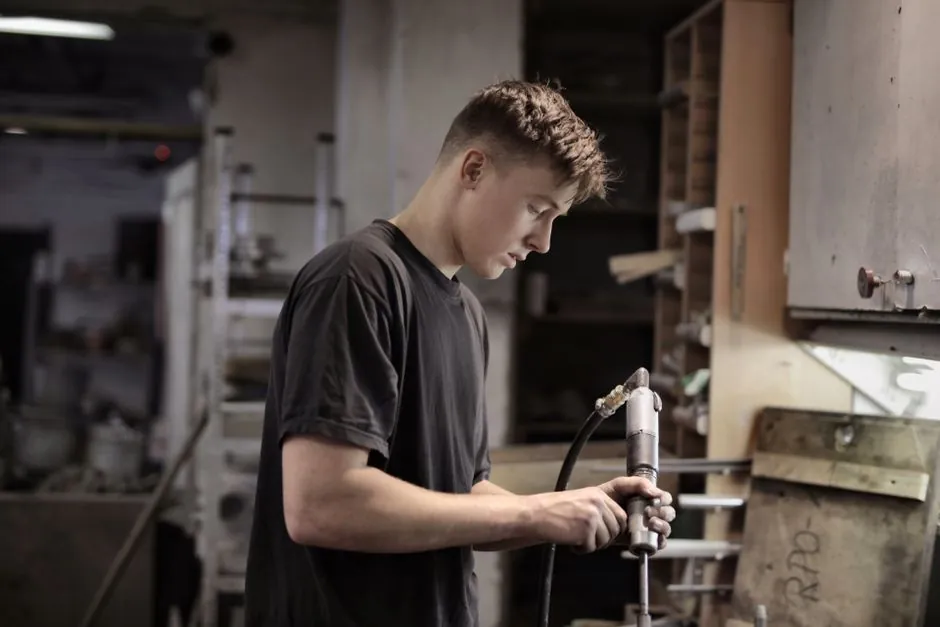
Moil point bits concentrate impact energy into a small area for hard rock and concrete penetration, while flat chisel bits spread force along a wedge edge for trenching, asphalt cutting, and controlled splitting. Match bit geometry to material hardness, rebar content, and break pattern; mismatched t
Air impact wrenches for indoor shop use typically measure 85 to 105 dBA, with quiet 1/2" models sitting at 85 to 89 dBA and budget or high-speed units reaching 105 to 112 dBA, well above the 85 dBA NIOSH 8-hour exposure threshold without hearing protection.
Heavy-truck lug nuts typically need 200-500 ft-lbs of tightening torque, so a 3/4-inch drive air impact wrench rated 600-1,000+ ft-lbs is the safe minimum. For severe service (1-inch drive, mining/agriculture lugs), 1,000-2,200 ft-lbs pneumatic wrenches are common.
Air-pick chisel shanks fall into two families: round (cylindrical) and hex (typically 1/4 in / 6.35 mm quick-change), and they are not cross-compatible. Match shank geometry to the tool's collet or chuck before buying, or expect slip, runout, and accelerated wear.
Air pick (pneumatic breaker) rentals run $30–$80/day, $105–$280/week, while towable 185 CFM diesel compressors run $56–$255/day, $118–$892/week across U.S. rental houses in 2026.
Air impact wrenches deliver higher peak torque (up to 2,200–3,000 Nm / 1,600–2,200 ft-lb breakaway on 1-inch-drive models) but torque consistency drops with falling line pressure and hose length, while cordless electric impact wrenches hold repeatability better across the cycle at the cost of absolu
An adjustable (crescent) wrench's moving jaw carries a higher slippage risk than a fixed-size spanner because the design has measurable slack and lower torque capacity, with IS 6149 testing a 300 mm adjustable at 480 Nm versus 643 Nm for a comparable fixed open-end and 884 Nm for a box/ring spanner
Hand-arm vibration from air impact wrenches causes measurable wrist, elbow, and tool-handle accelerations (ISO-weighted means of 7.49, 4.05, and 6.26 m/s²), and design choices like twin-hammer mechanisms, polymer-isolated grips, counterweights, and rear exhaust diverters directly lower exposure and
For hard-joint bolting, twin hammer air impact wrenches deliver 1,220–1,400 BPM at 85–97.7 dBA while jumbo hammer models run one hard blow per revolution at 89 dBA, with mechanism choice dictated more by vibration, joint type, and torque than by noise alone.
For air impact wrenches in 2026, the practical split is friction (hog) ring for fast socket swaps, pin-and-O-ring for the most secure positive lock on 1/2" and larger drives, and pin/detent for steady-state high-torque work.
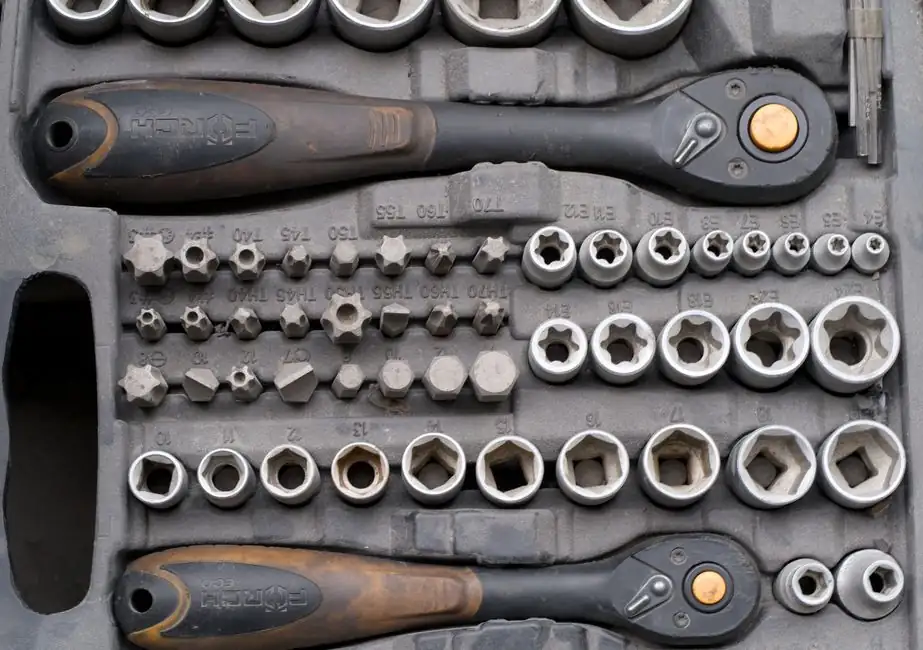
Chrome (Cr-V) sockets must not be used on impact wrenches: they are 30-50% thinner-walled, heat-treated for hardness, and shatter without warning under hammer torque. Impact sockets are Cr-Mo, 30-50% thicker-walled, and designed to deform safely; they are acceptable on hand tools but always required
Pin detent anvil retention delivers maximum socket security for high-vibration, high-torque bolting, while friction ring retention trades security for tool-free, faster socket swaps. Choose pin detent for jobsite and industrial work; choose friction ring for general repair and frequent socket change
Air impact wrenches are rated for approximately 90 PSI (6.2 bar) at the tool inlet, with 1/4" to 1" drive sizes consuming 2-15 CFM at that pressure. Sustaining rated torque output requires both correct pressure and adequate CFM delivery from compressor, hose, and fittings.
Air impact wrench free speed ratings span roughly 4,500 to 11,000 RPM across commercial models, with 1/4" to 3/8" compact wrenches running 7,000-11,000 RPM, 1/2" automotive models around 7,500-8,500 RPM, and 1" heavy-duty wrenches dropping to 4,500-5,000 RPM for higher torque output.
For rusted fasteners, an air impact wrench needs at least 650 ft-lbs of breakaway torque for heavy suspension work, with 1,000+ ft-lbs required for industrial/agricultural jobs; pneumatic models reach 1,500+ Nm (1,107 ft-lbs) where cordless wrenches plateau.
For pneumatic impact wrenches, 3/8-inch ID hose handles 1/2-inch drive tools up to 25–35 ft, 1/2-inch ID is the workhorse for runs beyond 35 ft, and 1-inch drive guns above 45 CFM need 3/4-inch or larger ID to avoid torque loss from line pressure drop.
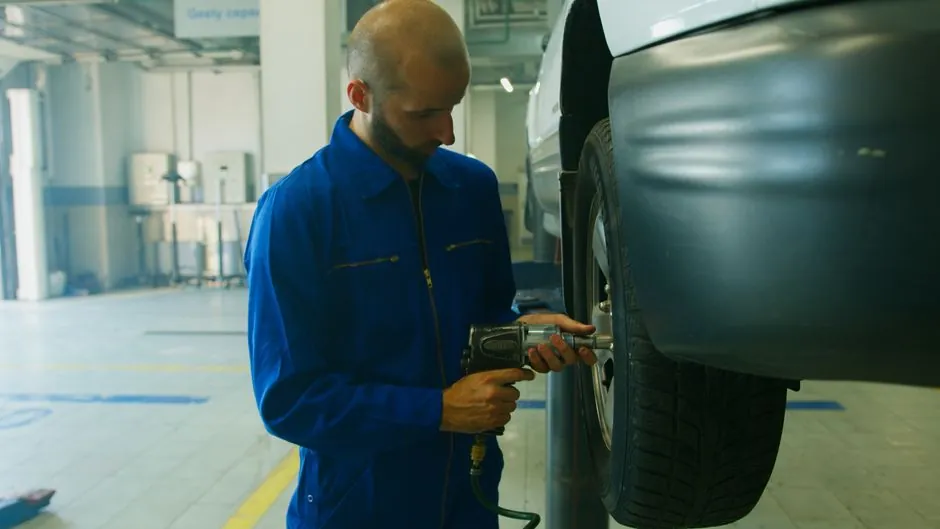
Extended-anvil air impact wrenches in 2", 3", and 6" anvil lengths are the standard answer for recessed lug nuts on cars, trucks, and tractors, pairing 1/2", 3/4", or 1" square drives with 425 to 2,100 ft-lbs of max torque. Choose 2" for passenger wheels, 3" for general shop reach, and 6" for deep-w
Air impact wrench total cost is driven mainly by drive size and torque class, not by brand or finish: 1/4 in tools sit at the low end, 1/2 in covers the 80-120 ft-lb automotive sweet spot, 3/4 in jumps to 1,200-1,600 ft-lb, and 1 in reaches 1,475-2,145 ft-lb, with material, hammer mechanism, and ATE
A 1/2" pneumatic impact wrench running continuously needs a compressor delivering 5–7 CFM at 90 PSI, paired with a 20–30 gallon receiver tank for 30–60 seconds of uninterrupted use before the pump cycles on. For shop-floor continuous duty, scale the tank to roughly 5–6x the tool's CFM, and oversize
Composite housings cut air impact wrench mass roughly 25 to 40 percent versus metal, while machined steel and magnesium shells still dominate shop-floor and heavy-bolting duty where impact shock and chemical exposure degrade polymers faster.
Air impact wrenches freeze in winter when two things fail at once: condensed moisture in the air line turns to ice in the exhaust, and the oil thickens past its pour point and starves the rotor. Switch to a winter-grade air tool oil (or a glycol-based antifreeze lubricant such as Kilfrost K400 or Su
A 1/2" pneumatic impact wrench needs 5-7 CFM at 90 PSI for continuous use, versus 4-5 CFM for intermittent (25% duty cycle) operation. Compressors should be sized 20-30% above tool demand, with continuous loads requiring average-CFM times four.
For tight-space fastening, a 1/2 in. right-angle pneumatic impact wrench (407 Nm, 1.4 kg, 90° head) outperforms pistol-grip tools on access, at the cost of reduced peak torque. Choose right-angle when access is the constraint; choose pistol-grip when peak torque and balance rule.
Air impact wrench rebuild kits typically run $30-$50 in parts with $50 shop labor, while a bare replacement costs $40-$150; rebuilds win on tools older than 20-30 years when a 4-7x life extension matters, but a $15 gap against a new unit with full warranty favors replacement for budget air tools.
For framing nailers run on hose, pressure loss at the tool is set by inside diameter, run length, and compressor CFM, not by hose length alone. A 3/8 inch I.D. hose at 50 ft with 90 PSI at the regulator delivers roughly 82–84 PSI at 100 ft; stepping up to 1/2 inch or shortening the run restores
Air hose length cuts impact wrench torque because pressure drop across a fixed inside diameter bleeds the 90 PSI inlet rating tools are spec'd at. A 3/8 in. hose suits most 1/2 in. drives up to 50 ft; above that, step to 1/2 in.; 1 in. drives need 3/4 in. or larger per Ingersoll Rand.
ACI 506R-16 defines three combined-aggregate grading bands (No. 1, No. 2, No. 3) with nominal maximum sizes from 3/8 to 3/4 in, and pairs each with air-content and quality requirements that govern nearly every North American shotcrete spec.
Acetylene reaches a higher neutral flame temperature in oxygen (about 5720–6300°F) and is required for oxy-fuel welding, while propane cuts the same ferrous metals at a lower flame temperature (about 5112–5122°F) and a lower cylinder pressure, making it the safer and cheaper default for cutting and
For cast iron welding, DC stick (SMAW) with a nickel (Ni-Fe) rod is the practical default: it gives a more stable arc, less spatter, and roughly 10 percent more penetration at the same amperage than AC. AC stick is reserved as a fallback for older transformer machines when magnetization or arc blow
Absolute encoders deliver true shaft position at power-up, making them standard in digital theodolites, while incremental encoders remain a budget option but require homing after every power cycle.
A 4D 16-line laser level projects four 360° planes (16 visible line edges) while a 3D 12-line unit projects three 360° planes (12 line edges), and the extra floor plane is the decisive difference for ceiling, drop-ceiling, and multi-elevation framing work. For single-room cabinetry, tiling, and pict
38 mm poker vibrators with 6 m flexible shafts span roughly USD 180 to USD 610 list price globally, with cost driven by drive unit, shaft alloy, and coupling standard. Electric 1600 W units cluster near USD 220, Australian heavy-duty assemblies list at AUD 279, and replacement Masterfinish shafts re
A 360-degree rotating base with a fine adjustment knob for line lasers is a mounting accessory that lets a line laser rotate freely around the plumb point while a micro-adjust knob dials the azimuth to sub-degree accuracy. Manual 1/4" and 5/8" thread bases start around $19.99, while motorised 3-spee

A 360° prism, built from six corner-cube reflectors, delivers omnidirectional EDM returns at roughly 1,500 m range, while a circular (single-face) prism extends range to about 3,000 m but requires aiming. Pick 360° for robotic tracking and dynamic layouts; pick circular for control traverses and pre
21, 28, and 30 degree framing nailers are not interchangeable: each takes a specific collation, and 28 vs 30 degree nails are usually safe cross-uses while 21 degree plastic strip nails will not feed in either. Pick by code (full round head), tight-corner access, and magazine capacity.
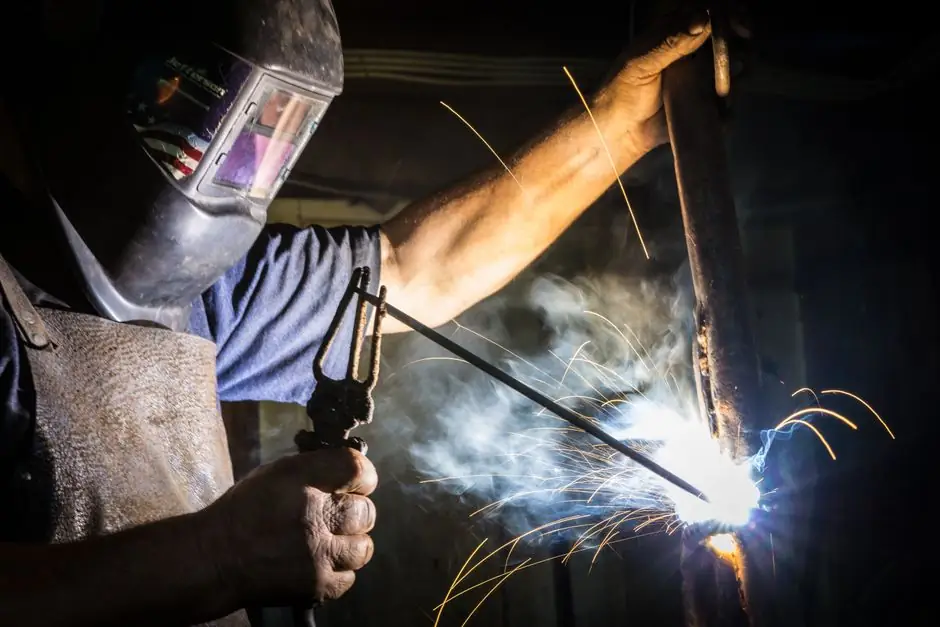
2% thoriated (AWS EWTh-2, red) and 2% ceriated (orange) tungsten electrodes differ sharply in current range, DC versus AC suitability, and radioactivity profile. Choose thoriated for DC steel/stainless at 150+ A and plasma work; choose ceriated for low-amp DC and AC orbital tube welding where 1.8–2.
For finish and trim work, 18-gauge brad nailers (1/2"–2" brads) suit narrow moldings, 16-gauge finish nailers add holding power for casing and baseboard, and 23-gauge pin nailers leave near-invisible holes for delicate assemblies where adhesive carries the load.
A 135° seismic hook is bent on a rebar bender by indexing the bend-angle stop to 135°, matching the central pin (mandrel) diameter to the code-required multiple of bar diameter (typically 4d for standard hooks, 6d for stirrups/seismic ties), and verifying the 6d straight leg extension after the bend
For UK and EU construction sites, 110V centre-tapped-to-earth (CTE) systems cap exposed voltage at 55V above earth, making them the de-facto standard for corded marble cutters. HSE guidance, not law, drives this choice. Choose 110V for wet, dirty, shared work zones; choose 230V only with 30mA/30ms R
Vibrator head diameter should be chosen to leave roughly 1.5–2.0 bar-diameters of clear gap on each side of the concrete vibrator head, with 25–35 mm heads for dense rebar zones and 50–60 mm heads reserved for wide, lightly reinforced forms. Use the 8–10× head-diameter insertion spacing rule and the
Digital levels read a barcoded staff electronically and routinely close loops under 0.01 ft, while automatic (optical) levels rely on manual visual reading of a graduated staff and are operator-dependent; choose digital for sub-mm precision and automated data capture, auto for low-cost general site
For sustained high-torque impact work above roughly 2,500 ft-lbs, a #5 spline drive impact wrench is the more durable choice over a 1 inch square drive, because the multi-tooth spline spreads load across more contact area and resists the corner-fatigue failures that destroy square anvils. Square dri
On air impact wrench spec sheets, "working torque" is the sustained tightening range (e.g. 5-50 ft-lbs) while "maximum reverse torque" is the peak nut-busting output, often 30-50% above the forward max. The two values describe different operating regimes and should not be compared directly when sizi
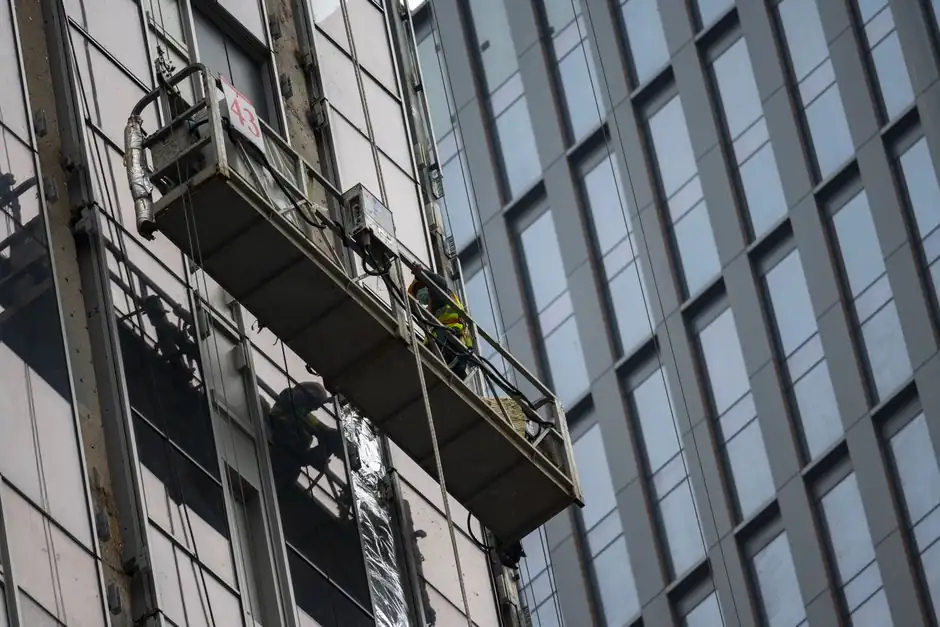
Wire rope suspended platforms suit low-rise facade work below 40 m with flexible rigging, while rack and pinion hoists dominate multi-storey construction for personnel and material lifts above 40 m. California Title 8 §1604.25 mandates a factor of safety from 7.60 to 8.40 on suspension wire ropes as
Mechanical rebar couplers are specified over lap splices in congested reinforcement because they transfer load bar-to-bar through a steel sleeve, eliminating the lap-zone rebar buildup that causes rock pockets, voids, and poor concrete consolidation, while meeting ACI 318-19 clause 25.5.7.1 capacity
Excessive spatter in stud welding is a symptom, not the disease. Root causes cluster in four buckets: misaligned current (too high or too low), contaminated or coated base material, a misaligned footplate or worn ceramic ferrule, and poor grounding. Fix the parameter and prep first, then the ferrule
Use internal and external vibrators together on tall wall forms whenever rebar congestion, deep lifts, or closed formwork blocks the poker from reaching the full cross-section. Internal pokers handle the bulk of consolidation; form-mounted external units cover the 5 ft × 2 ft influence band where th
An 8-foot aluminum step ladder is the standard pick for a 12-foot ceiling, giving roughly 12 feet of reachable height. Go to 10 feet if you want head clearance to stand two rungs below the ceiling while working overhead, and consider a 12-foot only for tasks requiring eye-level access to fixture box
For 3/4 inch (19.1 mm) headed shear connector studs, the stud welding power unit must deliver the drawn-arc current and time profile specified by AWS D1.1-20 and ICC-ES ESR-2856 (reissued October 2026), with field practice centering on 1,500-2,500 A at 25-45 V DC for 0.4-1.0 s weld time, supplied by
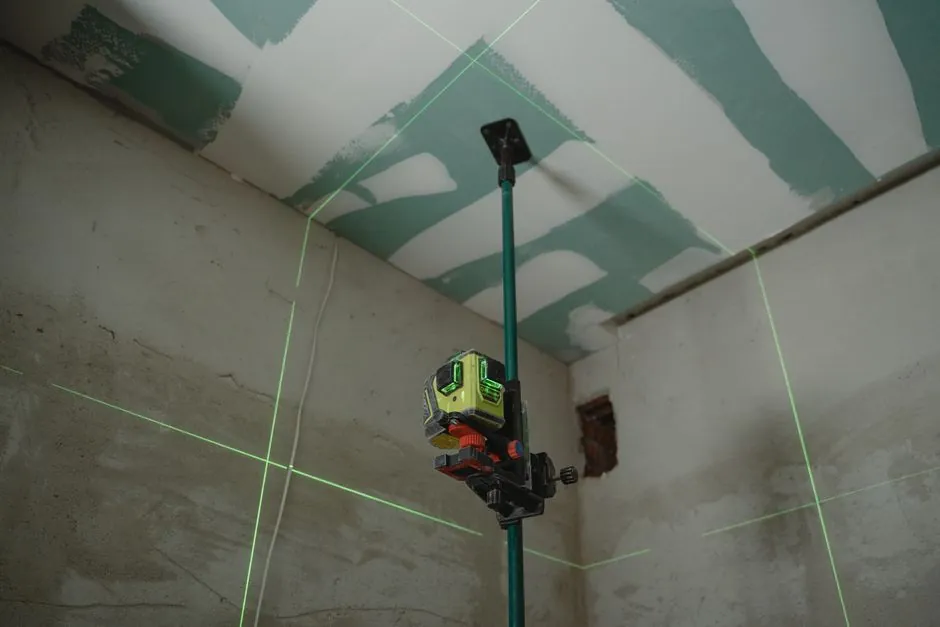
Laser distance meters calculate range by timing a laser pulse's round-trip to a target, using the constant speed of light to convert time into distance. Practical hand-held units cover roughly 0.05 m to over 100 m, with triangulation, phase-shift, and interferometric variants used for different accu
EN 1004-1:2020 caps freestanding mobile access towers at 12 m platform height indoors and 8 m outdoors, with stabilisers or outriggers mandatory above the lower limits. Towers exceeding these heights must be tied to a structure and fall under BS 1139-6 rather than EN 1004.
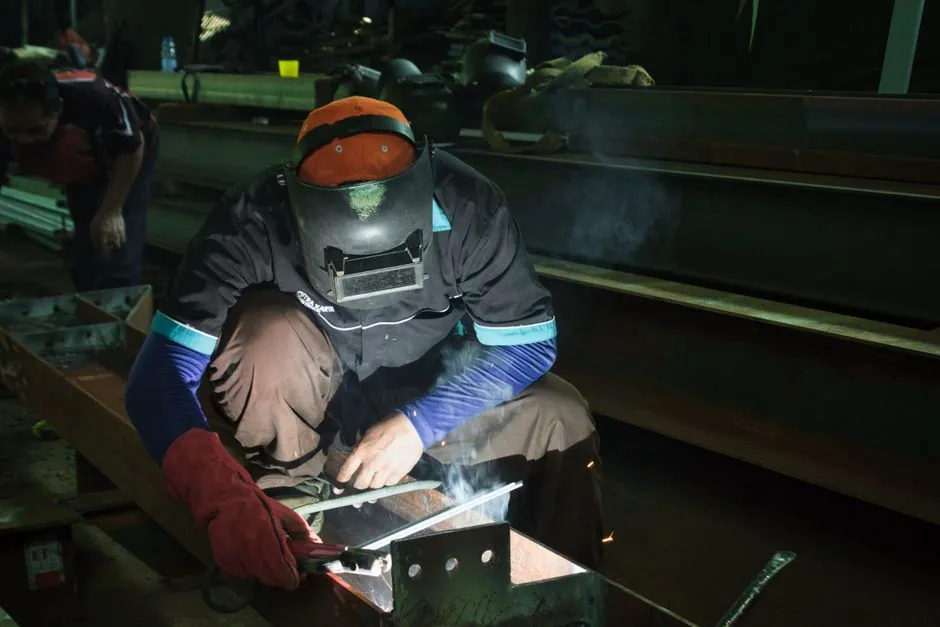
CD stud welding uses a stored capacitor bank charged from 110–115V AC to fire a sub-3 ms arc, joining small studs (typically ≤⅜" or M3–M10) to thin sheets. Drawn arc stud welding uses a DC power source (110V or 480V three-phase), runs 100–1,500 ms, and handles 3–25 mm structural studs on ≥1.2 mm bas
A laser distance meter is a general construction-grade time-of-flight instrument for measuring room, façade, and indoor distances, while a golf rangefinder is a specialised laser rangefinder with magnification, slope logic, and pin-lock algorithms tuned for targets at 5-400 yards. The two overlap in
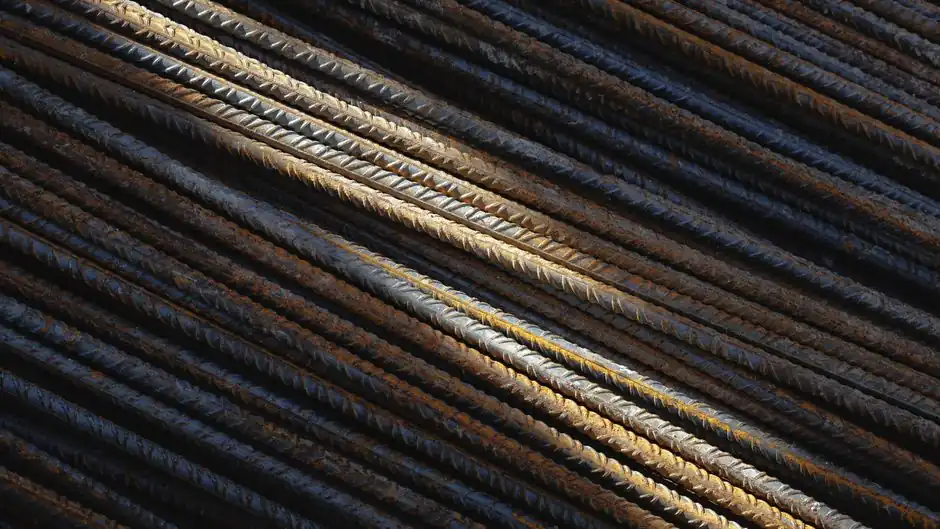
A bar bender fabricates reinforcement to the bending schedule, while a steel fixer places and ties it inside the formwork; in practice the two roles are combined under a single NSQF Level 4 trade qualification (CON/Q0203) covering both tasks.
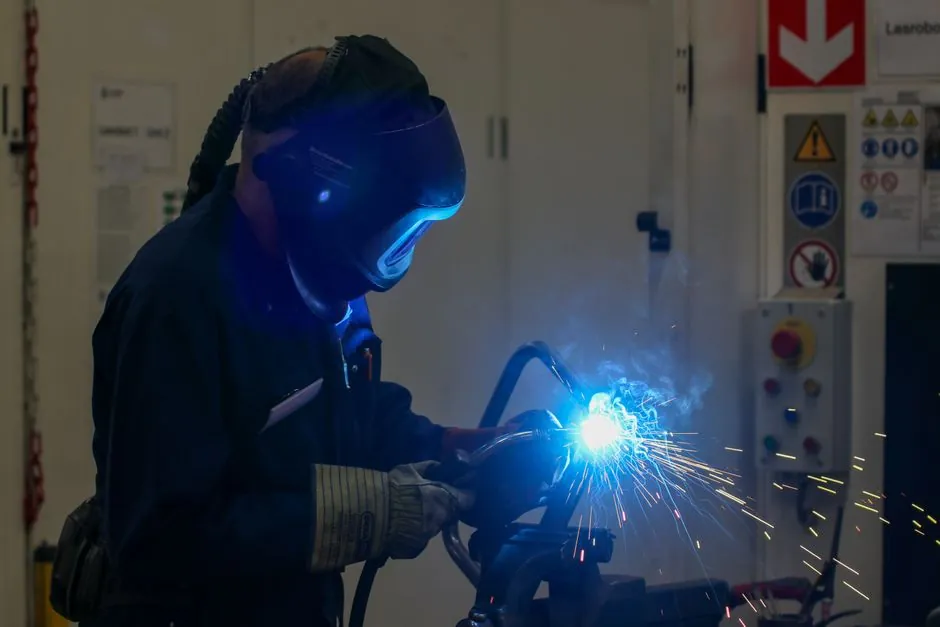
Arc force on an inverter MMA welder is a transient current boost triggered by a sudden arc-voltage drop, used to prevent electrode sticking and stabilise a short arc. It is distinct from Hot Start (ignition only) and Anti-Stick (post-stick shut-off), and the typical Hot Start envelope is 0.25–0.5 s
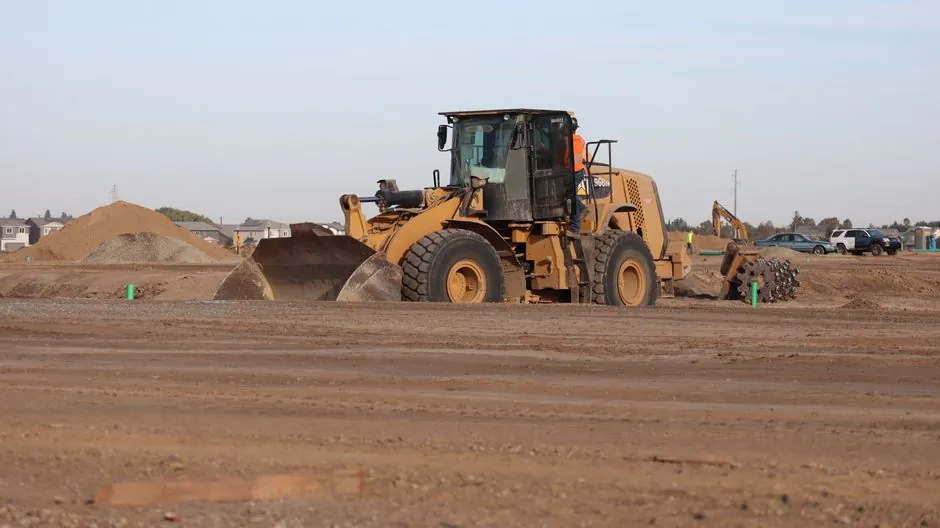
A rotary laser level on a grading job projects a self-leveled 360° reference plane across the site, and a detector on a grade rod reads that plane to drive cut/fill to a target elevation with accuracy between 1/16 and 1/8 inch per 100 feet depending on leveling method.
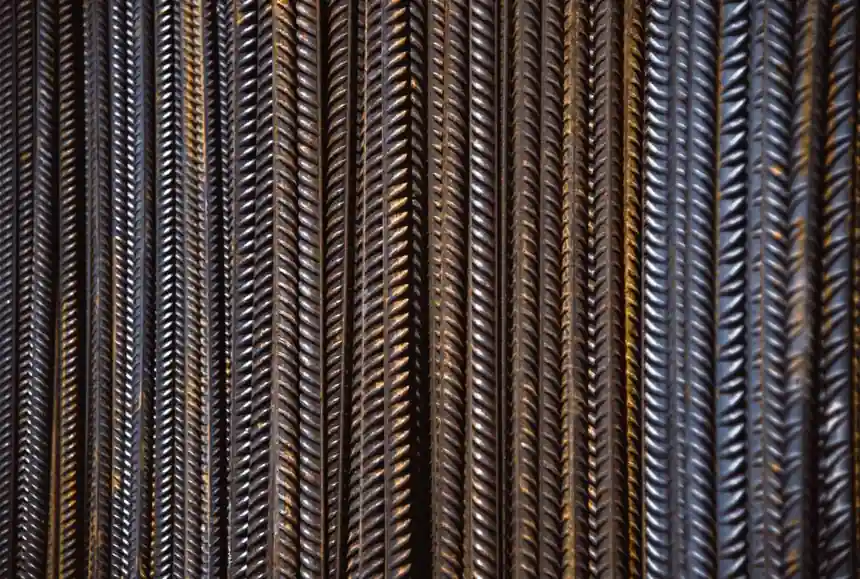
A rebar bender operator runs shearlines, table benders, auto-benders, and stirrup benders on a fabrication shop floor, setting up jobs, cutting and bending bar to spec, and tagging output for delivery.
An automatic level's compensator is a gravity-suspended prism or mirror that automatically redirects the optical line of sight to true horizontal after the user roughly levels the circular bubble, typically settling within 1-2 seconds via magnetic eddy-current damping.
For thick steel plate (above ~10 mm), the right disc diameter is 230 mm (9 inch) for handheld angle grinders and 355-400 mm (14-16 inch) for stationary machines, with disc thickness stepped up to 2.5-3.2 mm to survive lateral load and deep kerfs. Thinner 1.0 mm wheels on a 125 mm grinder su
Wet mix and dry mix shotcrete differ primarily in where water enters the mix: dry adds water at the nozzle, wet pre-mixes it. Each process has distinct equipment cost, production rate, rebound range, and ideal use cases, with selection driven by project scale, access, and stop-start frequency.
Welding machine duty cycle is the percentage of a 10-minute window the power source can deliver a stated output current before thermal protection forces a cooldown, with ratings governed by IEC 60974-1 at 40°C ambient. Higher amperage cuts duty cycle, so a 200A/60% machine cannot run flat-out for 6
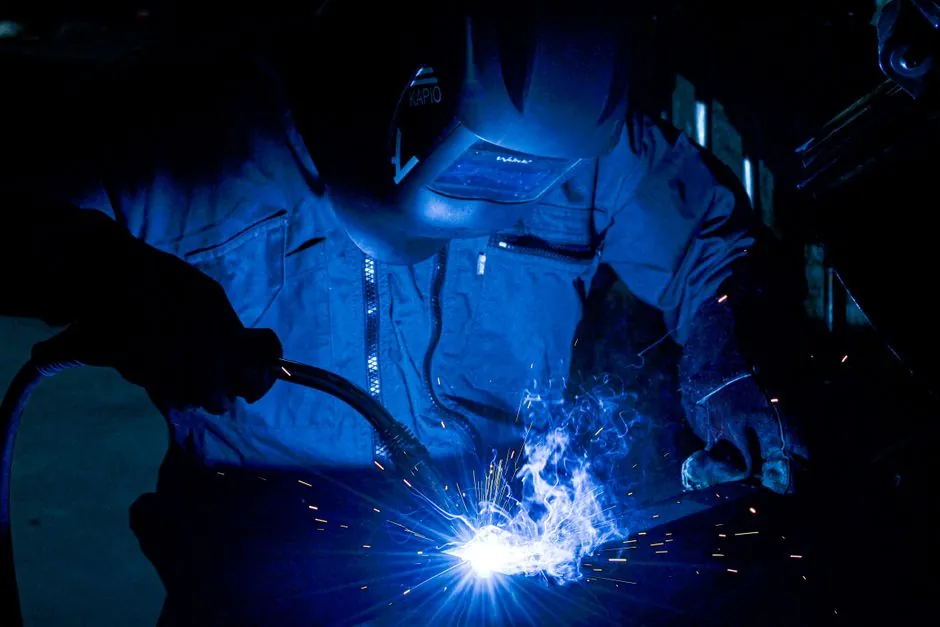
For a 6 mm stick electrode (1/4"), the typical MMA amperage range is 180-280 A, with 1 amp per 0.001" of steel thickness as the working rule. A 250 A-class machine covers this duty, while 200 A models are marginal. A welding machine specification for 6 mm work must also support a 60% duty cycle at t
External form vibrators on steel formwork are typically clamped at 3 to 6 foot centers, with insertion spacing about 1.5 times the vibrator's radius of action. Hold each insertion 5 to 15 seconds, keep the head 7-10 cm from the form face, and mount permanently to steel panels for predictable energy
Ride-on power trowels finish concrete roughly 3 to 5 times faster than walk-behind models, with quoted job-cycle gains of 30% to 50%, and cover up to 10,000 sq ft per hour on open slabs. Walk-behind units remain the only practical option below 1,000 sq ft, around doorways, and along edges where dual
A vibrating screed and a surface vibrator plate are not interchangeable: the screed is the workhorse for slabs up to ~15 cm thick, while surface vibrator plates are reserved for thin toppings, precast beds, and bridge-deck overlays where depth and tolerance control differ.
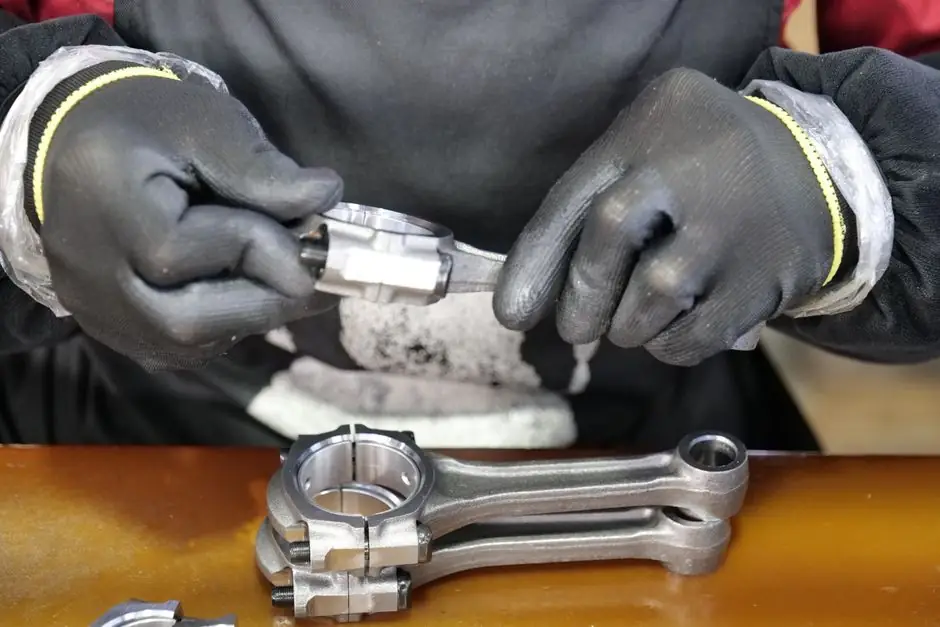
Urethane-tip and rubber-coated immersion vibrator heads protect epoxy-coated rebar and architectural formwork, while steel heads deliver higher impact force and lower cost. Choose urethane for tilt-up, low-slump, and rebar-sensitive pours; choose steel for general structural work and high-abrasion c
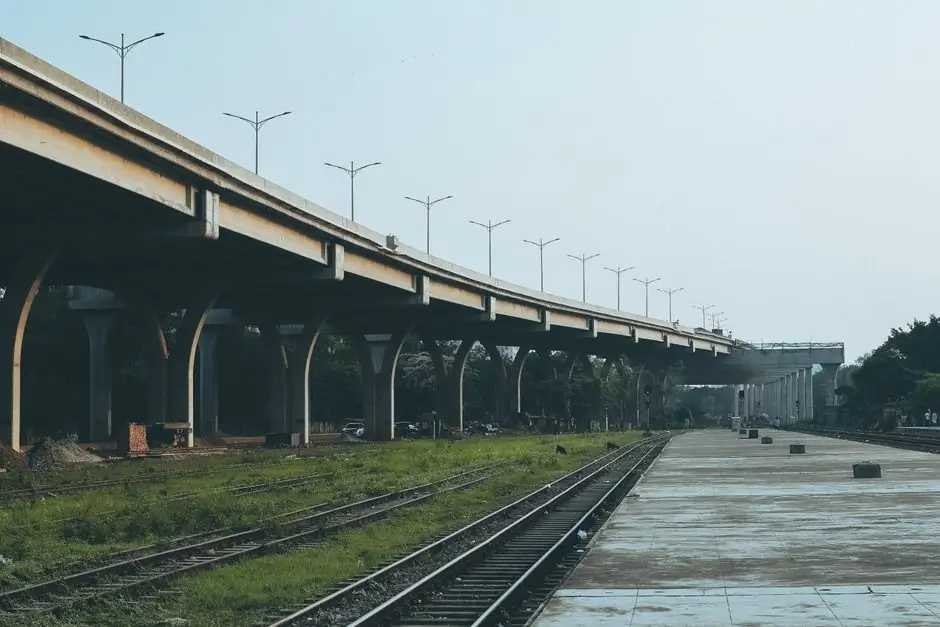
Underdeck suspended platforms and truck-mounted bridge inspection units serve the same soffit-access problem but diverge on rigging, reach, payload, and traffic footprint. Spec selection hinges on span length, ground access, and crew size rather than price.
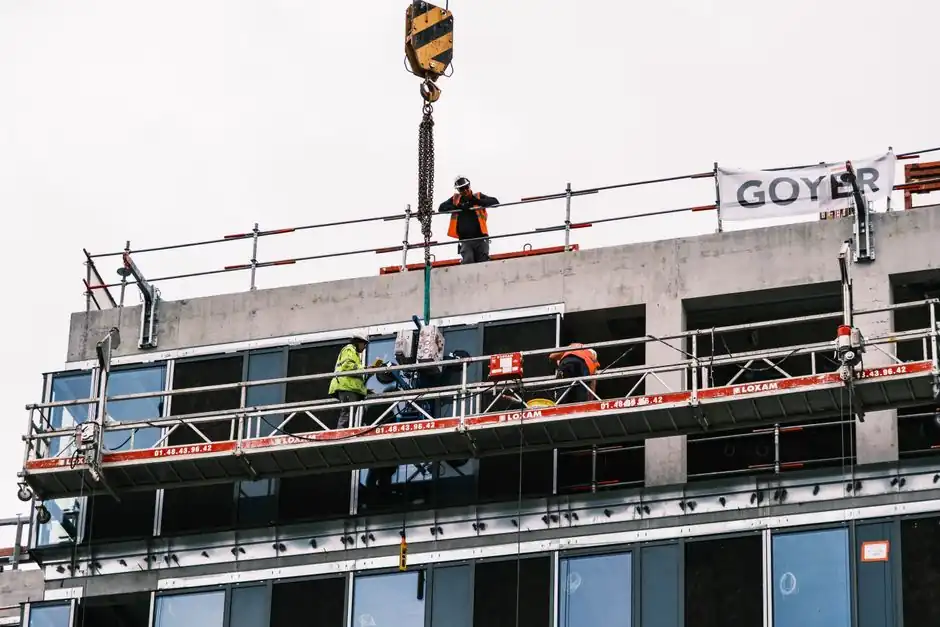
Underdeck suspended platform rail clamp load rating is governed by the support structure capacity rule: NYC Building Code 3314.10.2 requires parapet clamps, C-hooks, and outrigger beams to be supported by surfaces rated for 4x the imposed scaffold load, with 5,000 lb tiebacks and 5:1 factor-of-safet
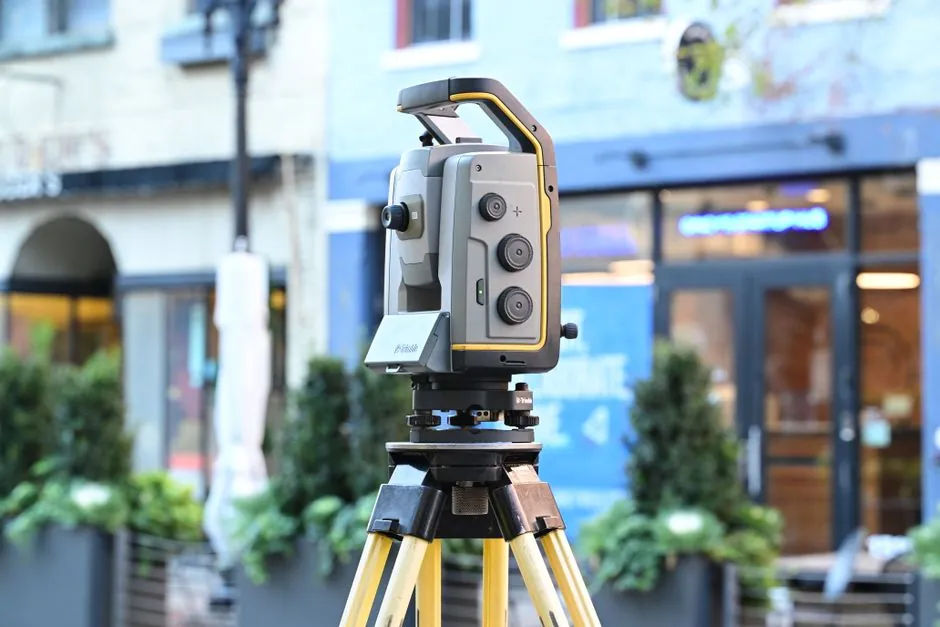
Survey-grade automatic levels deliver standard deviation of about 1.0 mm per kilometer of double-run leveling, with 0.2 mm/km digital flagships like the Leica LS15 and 1.5 mm/km optical workhorses like the Topcon AT-B4A spanning the practical range.
Type 1 mechanical rebar couplers must develop at least 125% of the bar's specified yield strength (1.25 fy), while Type 2 couplers must additionally reach 100% of the specified ultimate tensile strength (1.00 fu). Use Type 1 in low-seismic OMRF/IMRF members and standard column splices; specify Type
Two-speed percussion drills use a low gear (typically 0-450 RPM) to deliver high torque for large-diameter bits in masonry, concrete, and thick steel, with low gear reducing rotational speed to multiply twisting force for clean hole starts and reduced bit wandering.
A transit theodolite is a theodolite whose telescope is short enough to rotate a full 360 degrees about the horizontal trunnion axis; "transiting" is the act of flipping that scope through the zenith to enable back-sighting and angle doubling.
Rotary laser level elevation transfer projects a self-leveled horizontal plane from a benchmark, reducing transfer time by 60-70% versus optical leveling across 400-800 ft diameters. Best-fit type depends on slope: self-leveling (flat), single-grade (0-10% one axis), or dual-grade (±10% dual axis).
Air impact wrenches lead torque-to-weight class by ~150-250 ft-lb/lb on 1/2" drive pistol-grip builds, per published tool specs and side-by-side reviews through 2026-10-05. Cordless 1/2" models cluster at 47-114 ft-lb/lb depending on battery platform; hydraulic stays below pneumatic in weight ratio.
A standard TIG torch cable combines power conductor and shielding-gas hose inside one jacket, using a 35-50 mm Dinse-style power connector at the welder end. Connection method depends on air-cooled or water-cooled torch series (17/18/20/26).
TIG foot pedal wiring is not standardised: a 5-pin plug may carry torch control on pins 3/5 with the potentiometer on 1/2/4, while Lincoln TIG 200 swaps the wire colors and a Vulcan unit uses a 9-pin Weipu SP21 with only 5 wires. Pinout must be verified per machine before any cross-brand swap.
DINSE bayonet connectors (200–600 A+) outperform Euro and Tweco torch connections for TIG duty above 400 A by lowering voltage drop and resisting vibration, while Euro (150–400 A) wins on quick-swap MIG convenience. Choose DINSE for automated, water-cooled, or thick-section TIG; choose Euro for gene
Theodolite angular accuracy is rated in seconds of arc: entry digital models publish 5 to 10 arc seconds, mid-range workhorses sit at 2 to 5 arc seconds, and geodetic-grade instruments reach 1 arc second or tighter, with the angular limit controlling traverse, alignment, and deformation-monitoring t
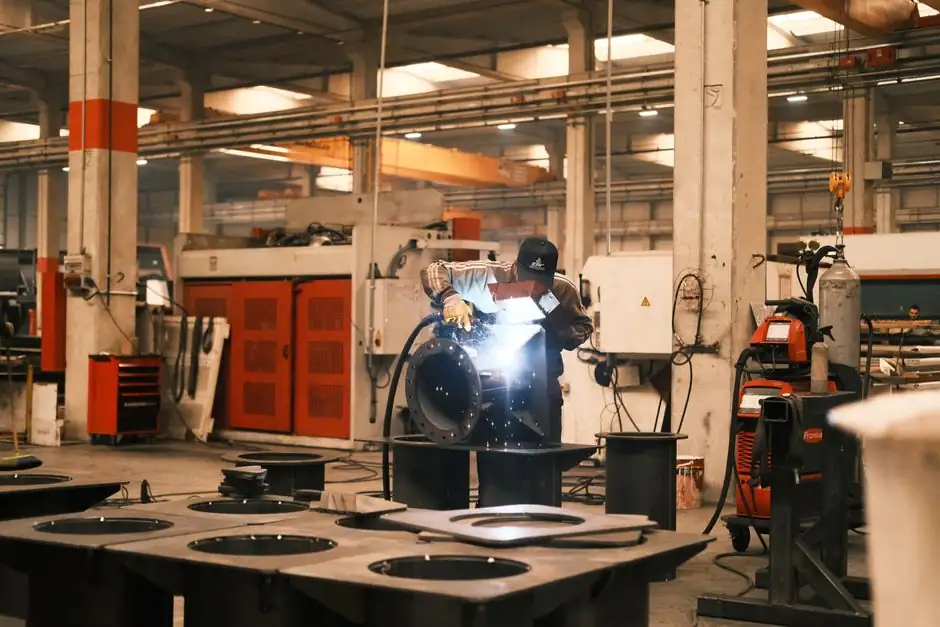
Stud welding diameter capacity spans #4-40 (about 2.8 mm) for capacitor discharge (CD) up to roughly 1-1/4 inch (32 mm) for heavy drawn-arc units, with the working envelope set jointly by stud material, base material, and process family per AWS D1.1 and DIN EN ISO 13918.
Stud welding and resistance projection welding are the two dominant methods for attaching fasteners to sheet metal, with the choice driven by one-side access, base-metal thickness, and cycle-time targets. Projection welding is the most common method for nut and M- or T-bolt attachment and typically
Stud welders split into single-phase capacitor-discharge units (110/230 V, 500–3000 W typical draw) and three-phase drawn-arc units (400 V 32 A, up to 1400 A welding current). Choose single-phase for portable/offsite work on studs up to 10 mm; pick three-phase when the weld schedule needs longer dut
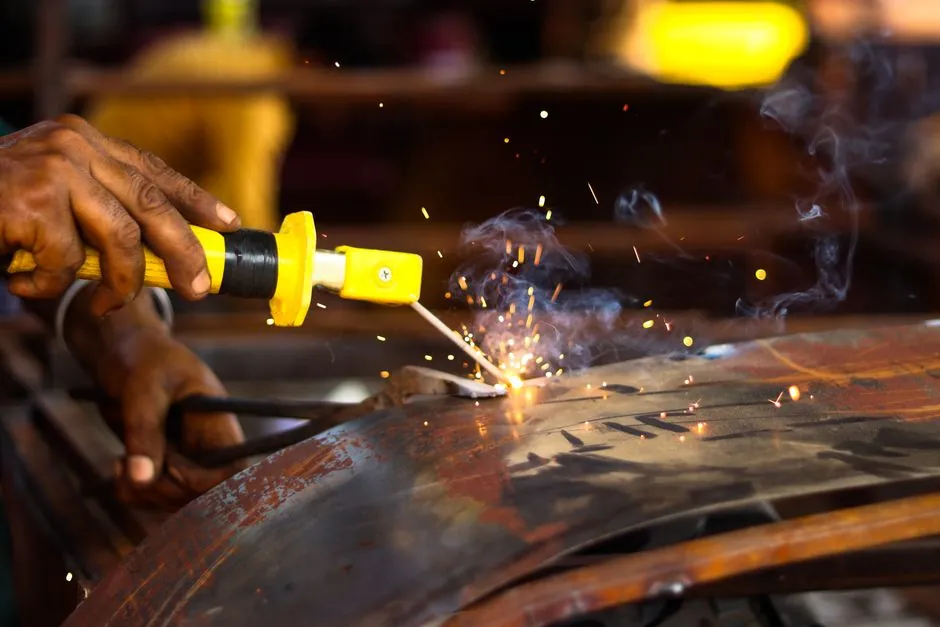
Capacitor discharge stud welders bank energy in a capacitor bank sized to the stud's weld base diameter: 3/16" to 7/8" studs are the practical CD range, with 1/8"-5/16" plunge and weld cycles under 10 ms.
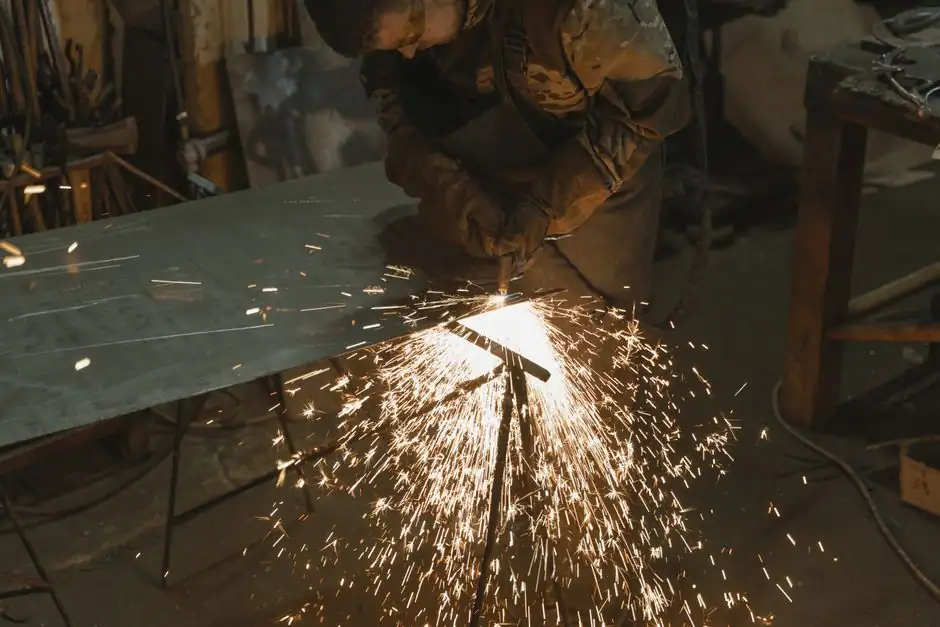
Stud welding power comes in three topologies (transformer, generator, inverter) and two process families (arc, CD). Real alternatives to a fixed-output CD unit now include 110 V inverter arc welders, M18-battery DIY CD banks, and cordless powder-actuated drivers, but each imposes hard limits on stud
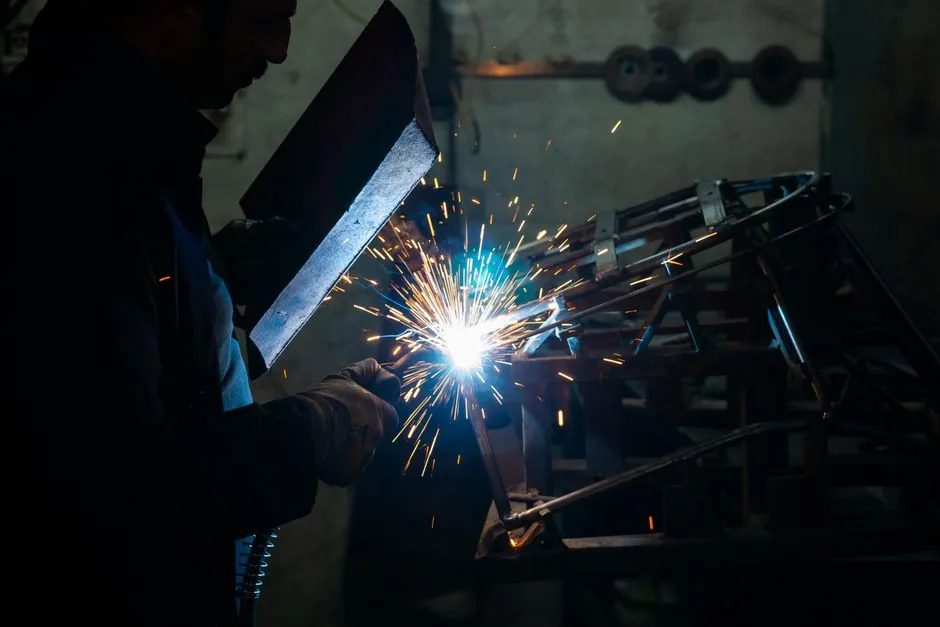
Portable stud welding power units (110 V, ~40 lb inverter/inverter-generator class) now cover up to 3/8" diameter drawn-arc jobs that historically required 3-phase shop power, while bench-mounted transformer and inverter systems still hold 17–45 V / 55–590 A continuous output for production lines.
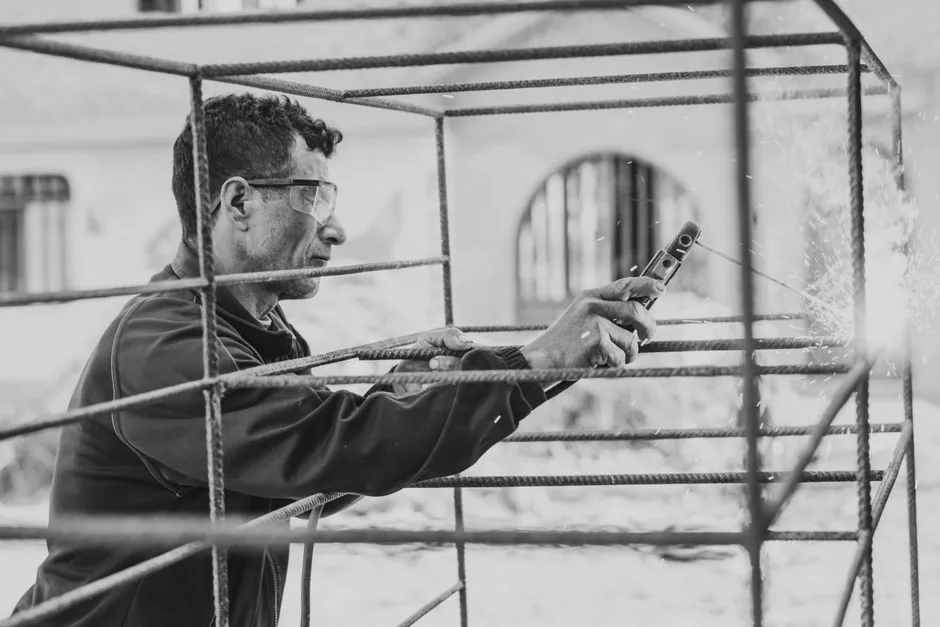
A clean stud weld depends on a precise gun trigger sequence: contact, lift, pilot arc, weld-time arc, plunge, and hold. CD welds finish in about 1 to 6 ms, drawn-arc welds run 100 to 1500 ms with typical 1/8 in plunge and 3/16 in for vertical walls.
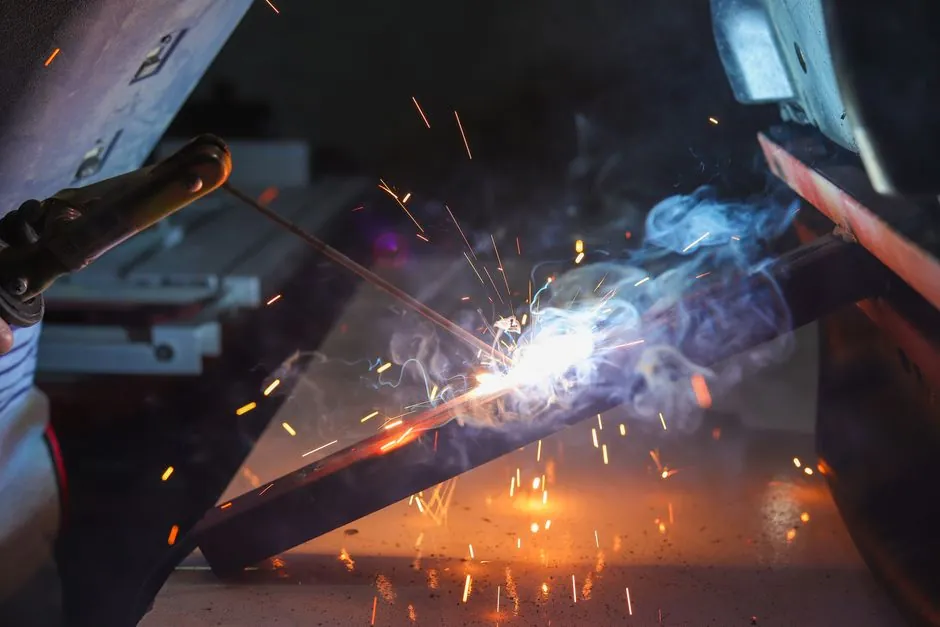
The ceramic ferrule in drawn arc stud welding acts as a single-use arc shield and mould: it contains the molten pool, blocks atmospheric oxygen, concentrates heat, and shapes a uniform fillet around studs typically 3–25 mm welded at currents up to ~3,000 A. Short-cycle and CD stud welding skip it in
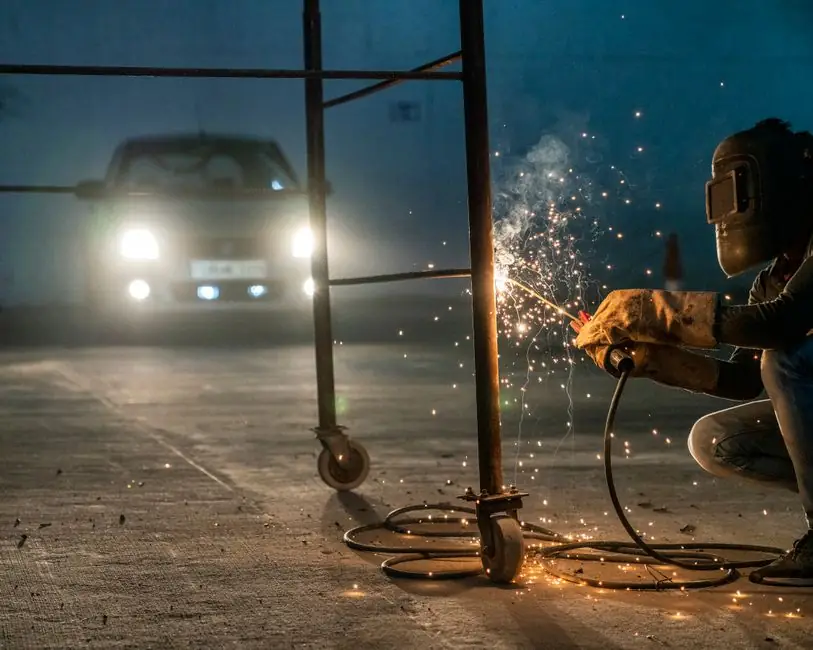
For stud welding, the practical minimum base-metal thickness to avoid burn-through is roughly 1.0 mm for thin-gauge mild steel using a low-energy CD process, rising to 2–3 mm for stainless and 3 mm or more for drawn-arc on heavy studs. Below those limits, the surrounding metal cannot sink enough hea
Wet-mix shotcrete typically loses 10-20% material to rebound on vertical work, versus 20-40% for dry-mix (gunite) under the same conditions. Floor and slab placement cuts that to 2-5%, but overhead work still hits 10-15% regardless of process. The trade is rate: wet-mix places 15-30 yd³/h against 1-
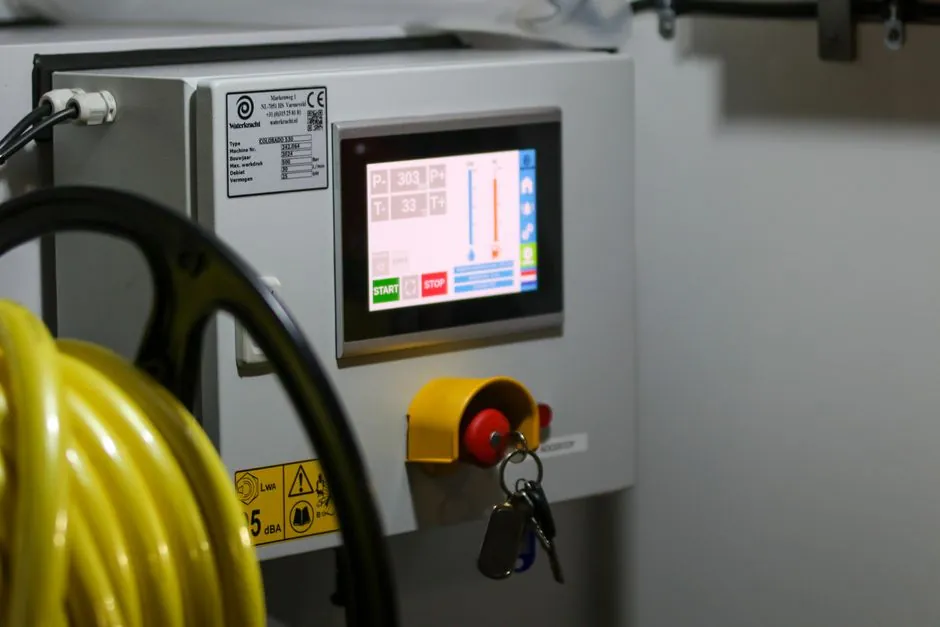
A mechanised wet-mix shotcrete rig is built from six functionally distinct sub-systems: concrete pump, spraying arm, additive pump, air compressor, chassis, and control system, each sized against a defined duty point. The biggest specification trap is the air/nozzle pairing, because compressor flow
Short-cycle drawn-arc stud welding without a ceramic ferrule is generally limited to stud diameters up to 8 mm, with the wider ferrule-free short-cycle envelope extending to 12-16 mm on thin sheet. Above 12 mm the consensus shifts to drawn-arc with ferrule or shielding gas to control the arc and poo
Shear-bolt couplers suit existing bars because they need no bar-end prep, while threaded couplers deliver higher cyclic and Type 2 tensile performance but require threading or upsetting the bar end. For retrofit work with limited access, shear-bolt systems win on install speed; for new high-capacity
Semi-automatic cold saws with hydraulic feed control bridge manual and full-automatic cutting, suiting low-to-medium production runs. Manual saws fit short custom work, while semi-auto models like the Dake 350 SA (14-inch blade, 20–105 rpm) handle 4-inch-and-under material at lower cost than full au
Self-leveling rotary laser levels typically deliver ±1/8 inch accuracy at 100 feet (about ±3 mm per 30 m), roughly double the working distance of manual units for the same error band. Self-leveling is the right pick for crews needing single-operator productivity, while manual leveling still fits tig
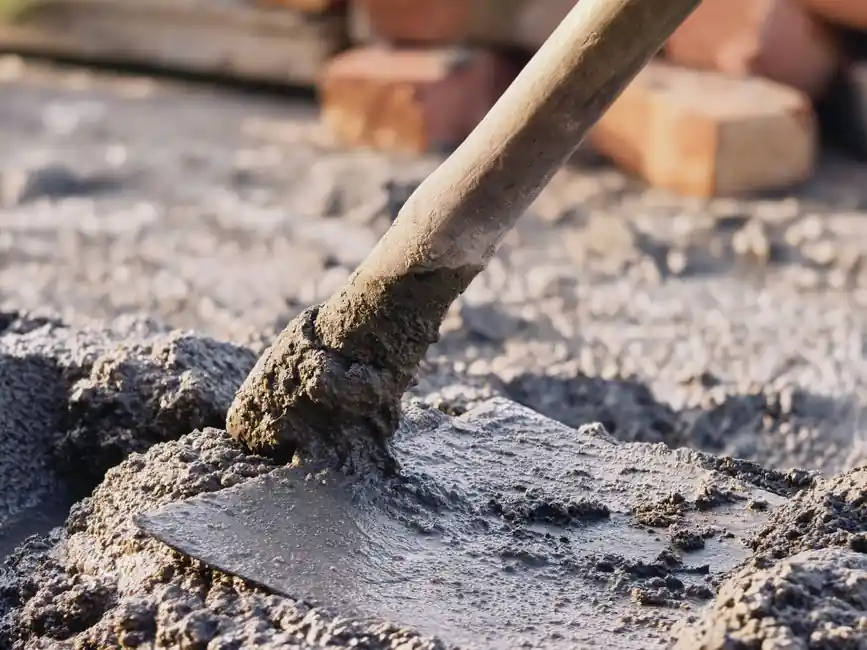
Rubber-tipped concrete vibrator heads protect fusion-bonded epoxy-coated rebar (ASTM A775) by replacing steel striking surfaces with urethane dimpled covers. Operating at 12,000 vpm with a 10,500 vpm floor under load, Oztec RubberHead® designs meet DOT non-metal head specs for bridge, DOT, and parki
On dry-mix shotcrete machines, rotor wear plates and rubber friction pads are the two highest-wear consumables; regular inspection of bowl steel, rubber pad condition, and clamping force prevents costly blow-by and downtime. Spare-parts inventories should always stock bowl steel, conical spout liner
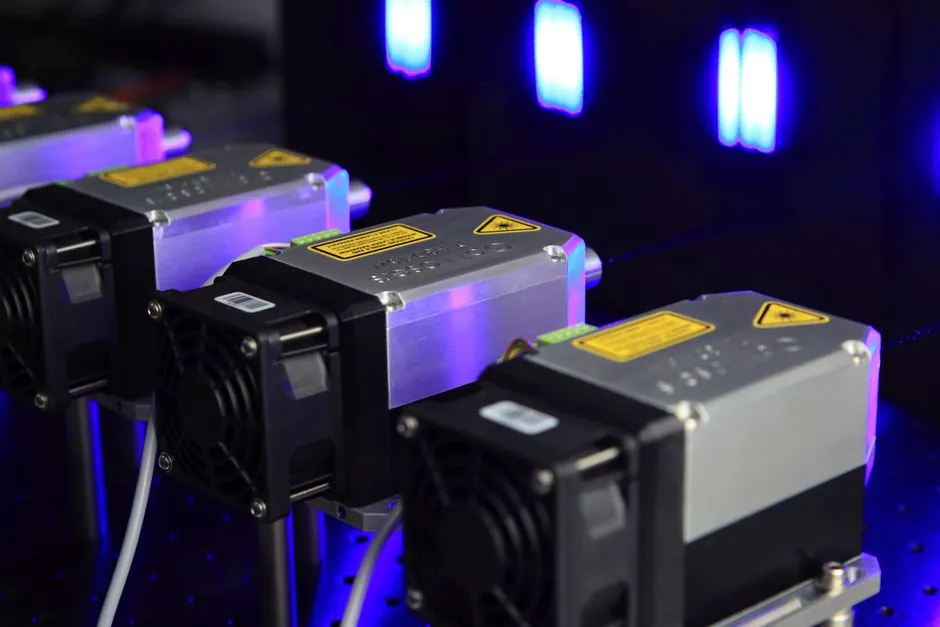
Rotary laser levels typically run $500 to $3,000+ while line lasers span $75 to $600, a 5-10x price gap driven by 360° rotating optics, 300-800m working range, and grade-slope capability; line lasers win on short-range interior layout at 15-50m with no detector required.
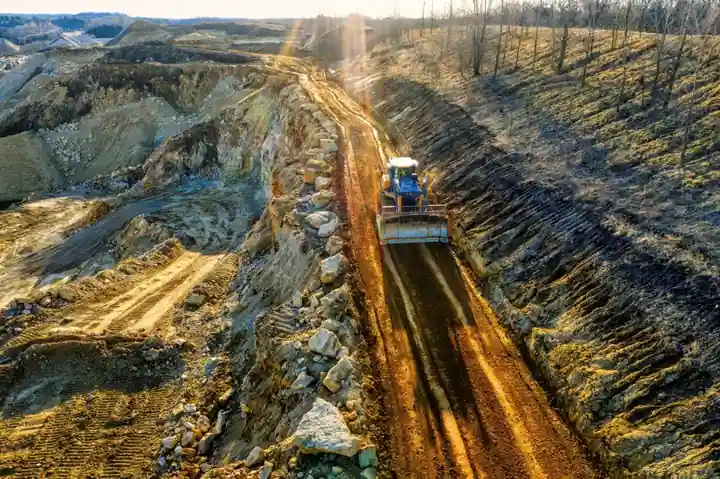
For site grading accuracy, rotary laser levels deliver ±1.5 mm at 30 m with 300–800 m detector range, outperforming line lasers (±1.5–3 mm at 5 m, 15–30 m visible range). Choose rotary for outdoor cut/fill and earthwork; line lasers stay inside.
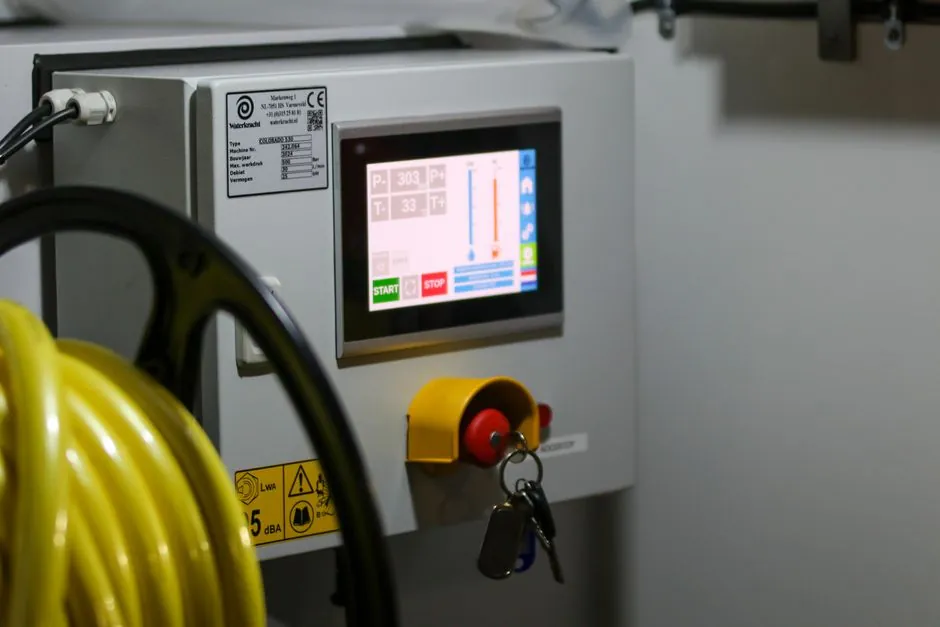
Remote-controlled power trowels for heavy slabs finish roughly 4,000 sq ft per shift, weigh around 90 kg (200 lb) versus 120-315 lb walk-behind units, and run on LiFePo4 battery packs with 200 rpm rotor speeds for zero on-slab operator exposure.
Refractory castable vibration is governed by three numbers on every job: layer thickness capped at 300 mm, vibrator spacing near 250 mm, and a short insertion window of roughly 15-30 seconds per point using a high-frequency immersion vibrator. Run the frequency too low or the time too long and you b
SS 310 V-anchors stud-welded to carbon-steel shells deliver reliable refractory retention to 1100°C, with anchor depth sized at 66-75% of lining and V/zig-zag geometry preferred over straight pins for thermal cycling.
Mechanical rebar couplers deliver roughly 125% of the bar's yield capacity at the splice and eliminate the development-length bond zone, so they win decisively over lap splices whenever the cage is congested, the bar is #11 (36 mm) or larger, or the splice sits in a tension member. Lap splices remai
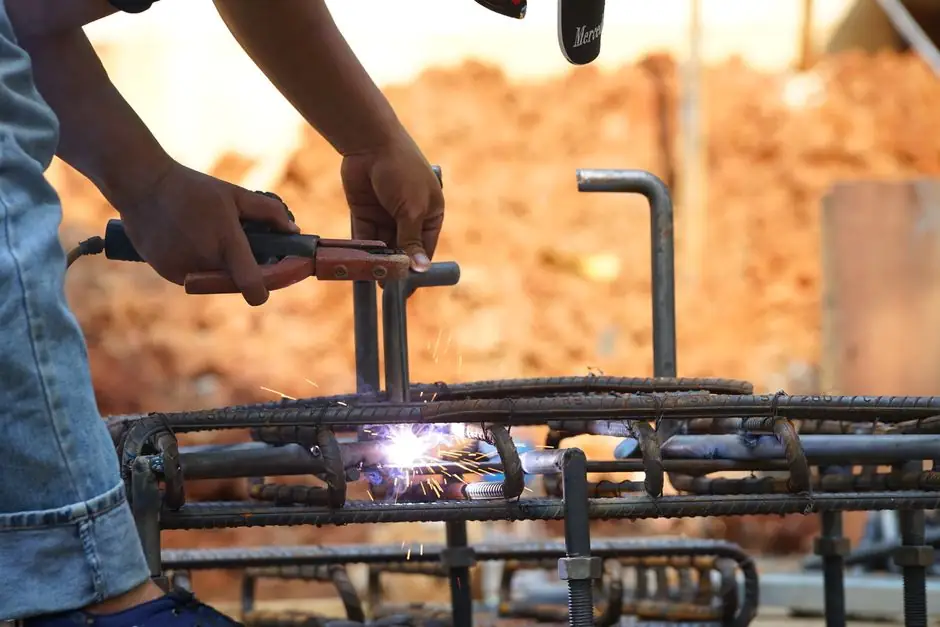
ACI 318-19 clause 25.5.7.1 requires mechanical rebar splices to develop at least 125% of the bar's specified yield strength (fy), with monotonic tension testing the principal qualification method per ASTM A370.
Swaged compression couplers deform a steel sleeve onto the rebar with a hydraulic press and need no bar-end prep, while threaded couplers rely on cut or upset threads and typically exceed 125% of ASTM A615 Grade 60 yield. Choose swaged for speed on large vertical column cages, threaded for seismic T
For a Type 2 mechanical rebar splice under ACI 318, slip is typically capped at 0.010 in. (0.25 mm) at 0.50·fy and at 1.00·fy, with full tensile strength of the spliced bar required. Slip tolerance is governed by the splice's seismic vs. non-seismic service class, not the coupler brand.
Standard parallel-thread rebar couplers scale from OD 24 mm x L 40 mm at bar size 16 mm up to OD 60 mm x L 92 mm at bar size 40 mm, with OD running ~1.45-1.5x the bar diameter and length ~2.3-2.5x. Imperial #4 through #18 bars follow the same ratio, ranging from 7/8" OD x 1-7/8" long to 3-1/8" OD x
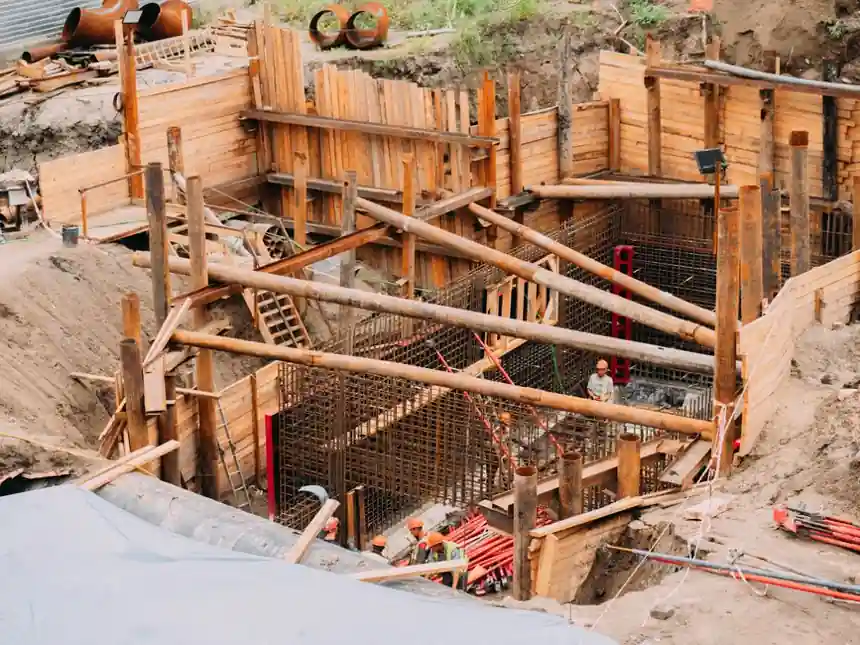
Mechanical rebar couplers are the default splice for bored pile cage section joints, delivering 125% of bar yield per ACI 318 clause 25.5.7.1 and eliminating the development-length congestion that defeats lap splices below cutoff elevation. Specify Type 1/2 splices for tension, taper-threaded or she
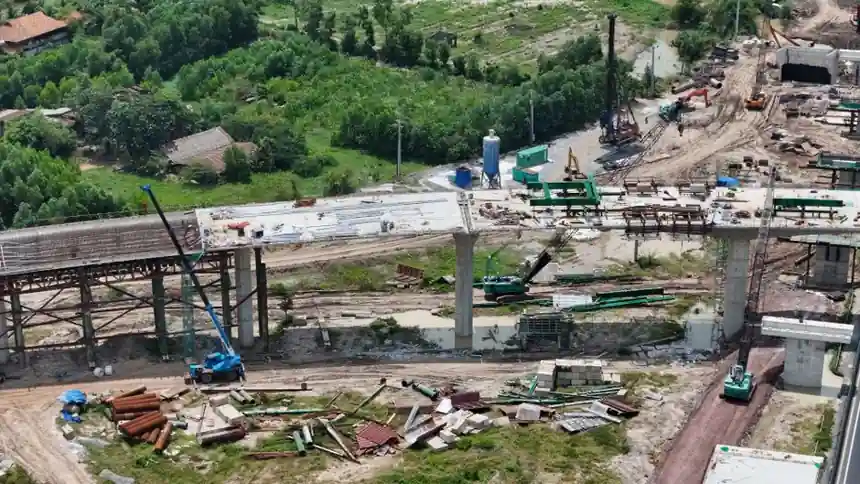
Mechanical rebar couplers typically deliver 20-50% total installed cost savings versus lap splicing, per industry studies. The per-splice coupler price is higher, but lap splice steel waste, code-mandated longer laps on epoxy-coated bars (up to 50% longer), congestion, and labor offset the unit
For a short rebar project under roughly 4-6 weeks of active bending, renting an electric rebar bender rated to 1 inch (#8) is usually the cheaper and lower-risk path versus buying. Choose purchase only when annual bending volume exceeds the rental break-even, or when the bar list and crew stay the s
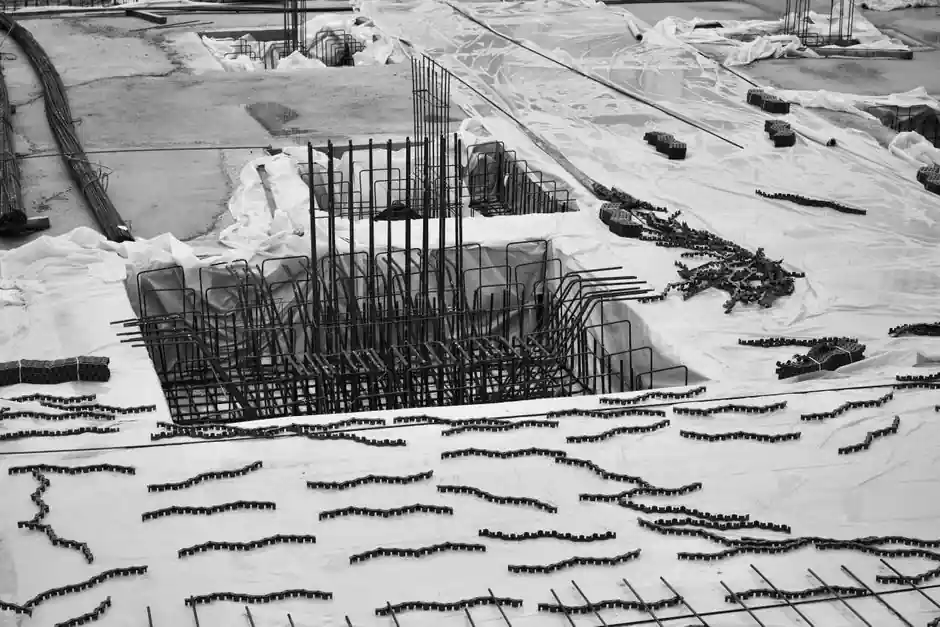
Reading cut and fill with a laser level and grade rod: set a rotary or self-leveling laser on a tripod over a benchmark, walk a grade rod fitted with a laser receiver across the site, and record rod readings to compute cut (remove material) or fill (add material) against the design elevation. A sing
Pre-dampener moisture for dry-mix shotcrete is capped near 5% by mass, because over-wetting lets cement stick to the hose wall and the pot bubbles back; the right range is "damp sawdust," not wet sand.
Poker vibrator head length sets the maximum single-pour layer depth: recommended layer depth is at most the head length, or up to 1.5x for eccentric-electric types, with layer-pour overlap above 300-500 mm. Common head diameters span 25-75 mm at 10,000-13,000 vpm, each producing a roughly 10x-diamet
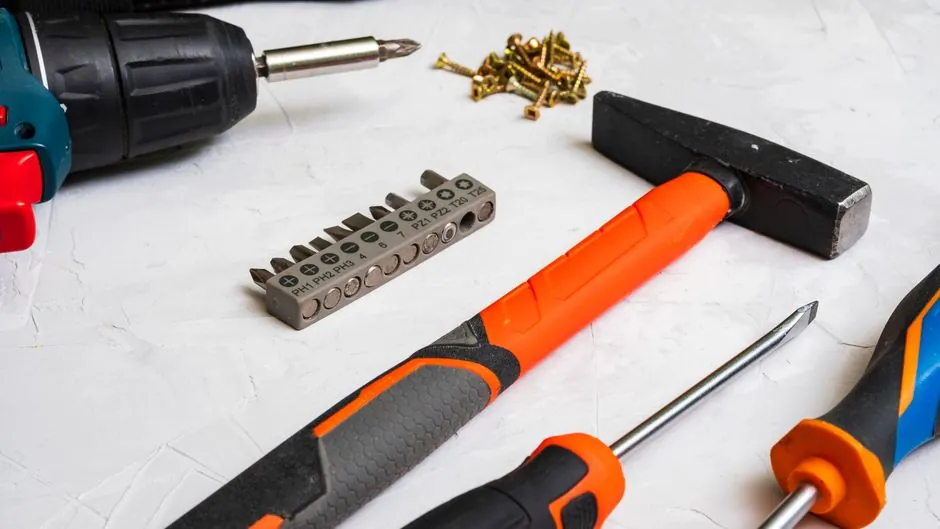
For masonry hole drilling, a standard drill with a carbide-tipped bit handles 2-3 anchor holes in soft brick or mortar, while a hammer drill is required for repetitive work, hard concrete, and large-diameter holes. The choice hinges on material hardness, hole count, diameter, and edge-clearance cons
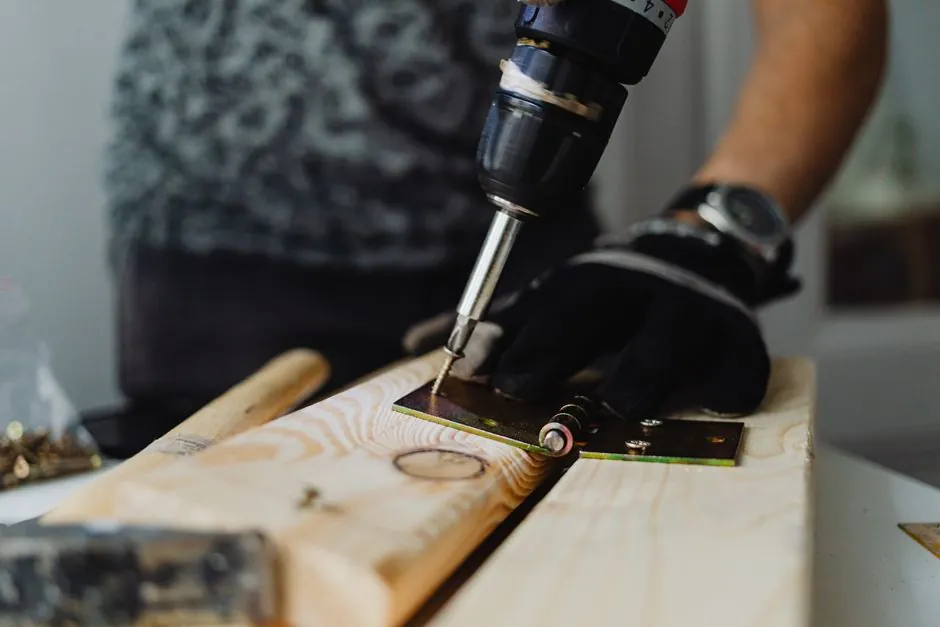
Percussion drills use a cam-driven ratcheting action that depends on operator feed force, while rotary hammers use an electro-pneumatic piston and striker that delivers discrete impact energy through an SDS-Plus or SDS-Max interface. The mechanism gap translates to roughly 2x the maximum concrete ho
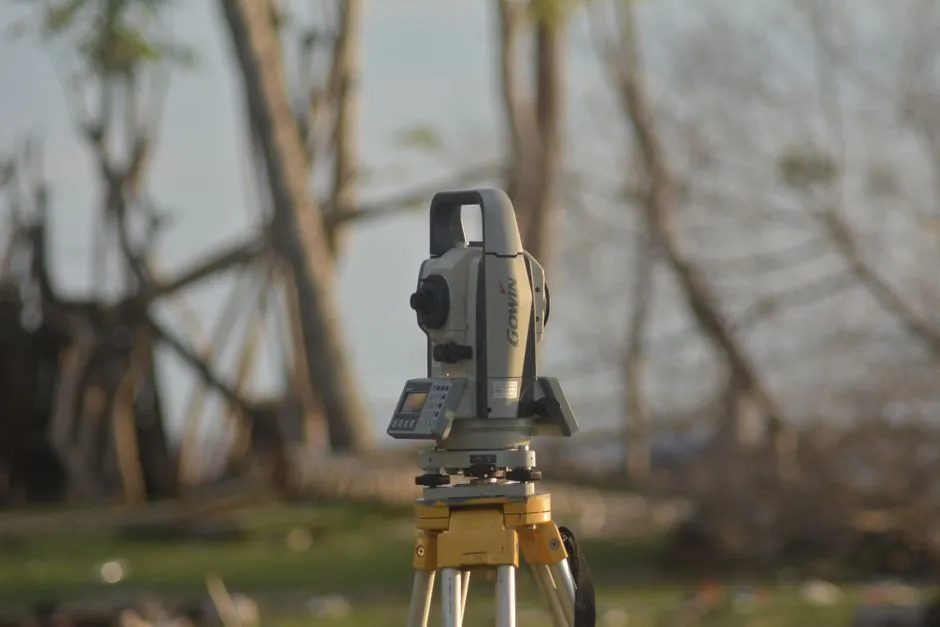
Inside an automatic level, the pendulum compensator and the prism compensator are not rival designs but two halves of the same gravity-referenced optical path. A pendulum-suspended prism (or mirror) hanging on fine non-magnetic wires is the active element that keeps the line of sight horizontal, whi
Parallel thread couplers (PTC) and taper thread couplers (TTC) install differently: PTC needs a locknut and full thread engagement, TTC self-aligns in 4 to 5 turns with a calibrated torque wrench. Choose TTC for speed and bar rotation freedom; choose PTC for higher tensile reliability, ~30% shorter
Overspeed safety lock calibration is mandated annually on elevators per EN 81-20/50 and ASME A17.1, with quarterly functional tests; suspended-platform OSL units trip at 30-42 m/min lowering speed and must be reset before each hoist shift.
Non-overlapping rotor ride-on power trowels lead the 2026 market with ~61% share versus overlapping designs, driven by higher torque for pans and finishing versatility. Overlapping units still win on seamless coverage at higher rotor RPM on wide slabs.
Optical theodolites read angles from graduated glass circles through a magnifying eyepiece with vernier or micrometer interpolation, while digital electronic theodolites replace that visual reading with optical encoders driving an LCD readout. Digital units consistently reach 2 arcseconds or better
Motor-in-head internal concrete vibrators place an electric drive motor and eccentric shaft inside the poker head itself, so the 42 V high-frequency stator is fed through a stationary-wire hose at 150 Hz or 200 Hz via a frequency converter, with no rotating shaft seal to leak. Cross-section stackup:
Phase-shift distance meters resolve the 2π ambiguity by combining multiple modulation frequencies: a low frequency sets the unambiguous range (e.g. c/2f), a high frequency sets the resolution, and coarse-fine or staggered schemes extend coverage up to 1.5–300 m in published laboratory systems.
Scaffold tower castor wheels in 2026 typically rate 400-1200 kg per wheel, with 6-inch and 8-inch diameters and 1-inch or 1-3/8-inch round stems dominating mobile tower builds. Total-lock brakes that hold both wheel and swivel are now the default spec, and engineers should divide total rolling weigh
Optical mechanical theodolites need scheduled vernier-and-bubble cleaning plus 6-12 month collimation checks, while electronic theodolites shift maintenance to battery contacts, encoder seals, and firmware, dropping field service to roughly once per year. Pick optical for remote sites with
Third-order differential leveling with an automatic level caps the maximum sight length at roughly 90 m (300 ft), with a typical 10 m balance limit between backsight and foresight, per WSDOT and FGCS-based guidance.
An arc welding power source is built from four core blocks: a primary input and isolation stage, a transformation or inversion stage, a rectification and smoothing stage, and an output control/feedback stage. Constant-current designs suit SMAW and GTAW, while constant-voltage designs suit GMAW, FCAW
A machine control laser receiver mounted on a dozer blade reads a rotating laser plane and tells the operator, or the hydraulics, where the cutting edge sits relative to finished grade. Indicate-only systems start near $500; automatic 2D dozer kits sit in the $10K to $25K range, with 1/4 in. accurac
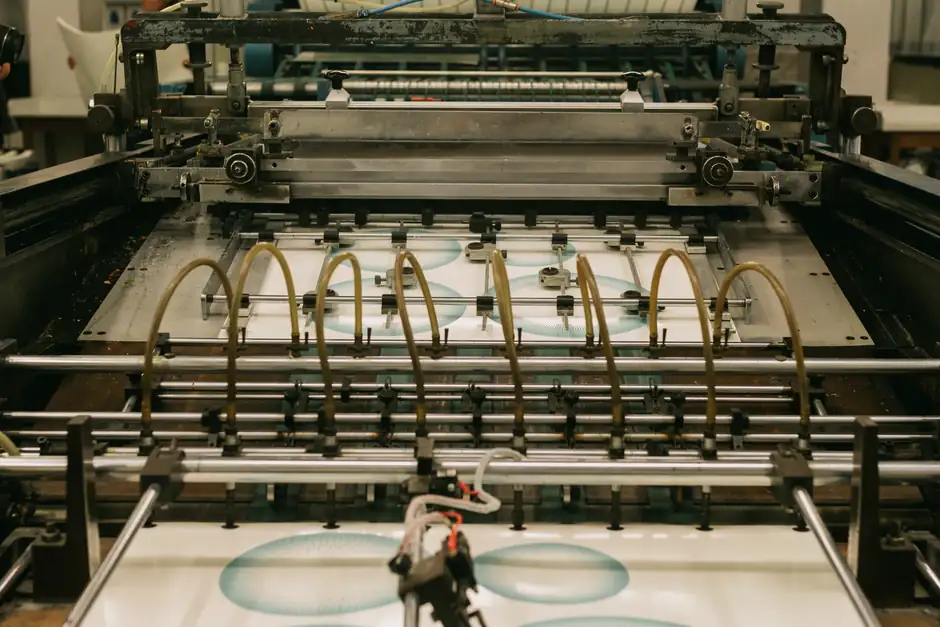
A length stop system on a cut-off machine is a fixed reference surface the workpiece butts against, holding cut-to-length tolerance to roughly 0.5 mm in production use. It scales from a scrap-wood block clamped to a worktable, through machined aluminum stop blocks on a crosscut sled, to engineered r
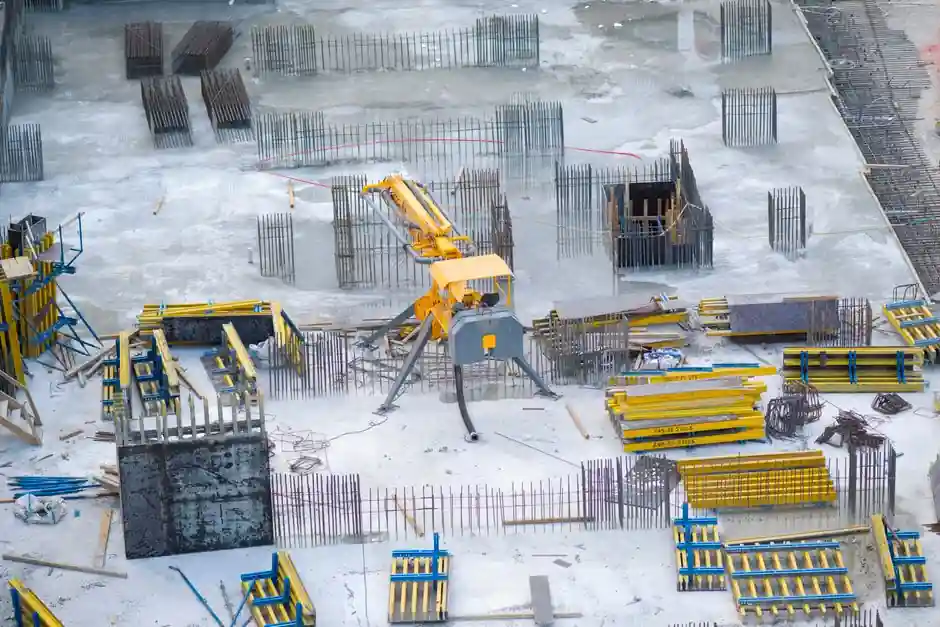
Laser screeds level roughly 240 sq ft of slab per minute (about 14,400 sq ft/hr) and cut finishing time to 3-4 hours per pour, while vibratory screeds cap at 15 cm (6 in) lift thickness and need a rail-guided double-profile setup above 3 m. Pick laser for pours over 4,000 sq ft; pick vibratory for s
A water level (clear hose + water, often 5/16 in to 3/8 in ID vinyl tubing) is the correct device for transferring an elevation around walls, trees, or buildings, while self-leveling rotary or laser level units deliver 1/8 in accuracy at 200+ ft only on an unobstructed line of sight. For a footing,
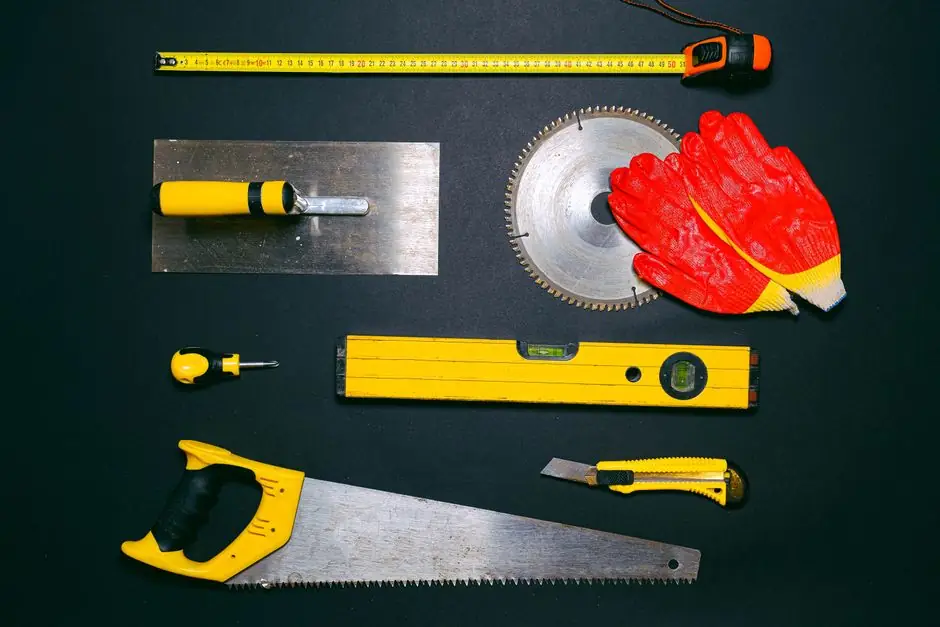
A theodolite measures horizontal and vertical angles with enclosed graduated circles, while a laser level projects a reference plane or line for one-person leveling. Choose the theodolite for angle and alignment work, and the laser level for fast, repeated height or plumb set-out on site.
Rotary laser kits ship as a matched crew: laser head, 5/8-11 tripod, receiver, and grade rod in one case. Outdoor work depends on the receiver; red vs green is irrelevant in daylight.
For drainage grading, a laser level's slope function is typically dialed in at 0.5% to 2% to move water reliably off a surface. Minimum practical drainage grade is 0.3%, while ADA ramps and highway caps push 8.33% and 3% respectively.
Green beam laser levels (505-550 nm) appear 3-4x more visible to the human eye than red (610-670 nm) and are the standard pick for outdoor daylight work, while red still wins on battery life and cost. Use a pulse-mode receiver whenever the line has to hold up past about 30 ft / 9 m in sun.
Outdoor grading relies on a rotary laser paired with a detector-mounted grade rod, with effective working diameters of 1,000–2,000 ft (300–600 m) and detection windows of roughly ±1 to ±4 in. Green beam, IP66 housing, and self-leveling are the dominant 2026 specs.
A laser receiver only works with a line laser if the laser emits a pulse-mode (modulated) signal, and the receiver must be tuned to the same pulse frequency and beam color, typically red 635 nm or green 520–525 nm. Huepar, Firecore, and Dovoh receivers listed in 2025–2026 catalogues all require puls
Dual-slope rotary lasers tilt the working plane on two independent axes, X and Y, while single-slope units only set one axis at a time. For drainage runs that fall in one direction a single slope is sufficient; for parking lots, sports fields, and roof drains that need a main fall and a cross fall,
Laser level accuracy tolerance at 30 m depends on the mm-per-meter ratio: a ±0.1 mm/m unit reaches ±3 mm at 30 m, while professional cross-line models stay within ±1/16 in (≈1.6 mm) per 30 ft and contractor rotary lasers hold ±1/16 in (≈4.8 mm) per 100 ft, with error scaling linearly beyond the stat
Time-of-flight (pulsed) laser distance meters reach 300 m to several kilometres at ±1 m accuracy, while phase-shift (modulated CW) meters stay inside roughly 0.1–200 m but hit ±1–3 mm, so the choice is range versus precision, not which is "better". Target surface, ambient light, and update rate then
Pulsed laser rangefinders reach beyond 30,000 m on non-cooperative targets with sub-nanosecond pulse widths, while continuous-wave (phase-shift) units deliver sub-millimetre accuracy over short ranges. Match the architecture to distance, target reflectivity, and accuracy budget.
ISO 16331-1 is the only public standard that defines how handheld laser distance meter range and accuracy must be tested, requiring both favorable (3 klux, room temp, white wall) and unfavorable (30 klux, full temperature span) conditions. It does not assign accuracy classes; users compare published
ISO 5468:2017 is the active dimensional standard for straight-shank rotary and rotary-impact masonry drill bits with hardmetal tips, covering 4–25 mm diameters in short, long and extra-long length series; it explicitly excludes hammer-drill (SDS) shanks, where PGM certification covers anchor-hole ac
ISO 16331-1:2012 specifies handheld laser distance meter range and accuracy under two defined conditions: favorable (3 klux ambient light, white painted wall, room temperature) and unfavorable (30 klux sunlight, white painted wall, full operating temperature range), enabling apples-to-apples compari
EN ISO 14555:2025 is the active reference for arc stud welding of metallic materials, approved by CEN on 3 August 2025 and superseding EN ISO 14555:2017. It defines quality requirements, WPS/WPQ, operator qualification, and production-weld testing for static and fatigue-loaded stud welds. Procuremen
Yes, a properly executed stud weld produces a metallurgical bond stronger than either the fastener or the parent material, while a drilled and tapped hole removes base-metal cross-section and caps load at the thread engagement area. Cycle time also differs by orders of magnitude: a drawn-arc or CD s
An impact drill and a hammer drill are the same tool; the term "impact drill" is a regional synonym for the percussive-action hammer drill, distinct from an impact driver, which delivers rotational concussive torque for fastening.
For stud welding power units, inverter-based machines deliver 20-30% better electrical efficiency, 50-70% lower weight, and faster arc response than transformer-rectifier units, but transformer-rectifier designs still win on 50+ year service life and tolerance for harsh field conditions.
Inverter arc welders deliver 80–85% electrical efficiency versus 70–80% for transformer-based machines, saving 10–20% power per the latest published comparisons. Choose inverters for portable, multi-process work and transformers for rugged, stationary, long-life duty.
Internal vibrators consolidate thick slabs, walls, and columns; form (external) vibrators drive energy through the formwork for precast, congested rebar, and high-finish members; surface vibrators (screed-type) suit shallow slabs under 150 mm. Choice is driven by member depth, rebar density, slump,
Under ASTM C31/C31M, the internal vibrator used to consolidate a standard concrete test cylinder must have a diameter no greater than one-fourth the diameter of the cylinder mold, and a minimum frequency of 9,000 vibrations per minute (150 Hz). For the common 6 × 12 in. (150 × 300 mm) mold that caps
Industrial-grade 1/2" air impact wrenches rated around 1,600 Nm outlast and overpower automotive cordless units peaking near 858 ft-lb, but they cost more, weigh more, and need a compressor. Pick industrial air for multi-shift production and heavy fastening; pick cordless automotive for mobility, li
Impact drill torque ratings span 40–80 Nm for general masonry use, while impact drivers reach 100–350 Nm and impact wrenches exceed 1,600 Nm. The Nm figure is rotational force, not raw power, and fastening torque is typically only 50–70% of the peak rating.
Keyless chucks and SDS chucks are not interchangeable: an SDS-Plus or SDS-Max bit will not lock into a 3-jaw keyless chuck, and a round-shank bit cannot seat the hammer mechanism of an SDS rotary hammer. Use keyless 3-jaw chucks for round or hex-shank bits, and SDS systems only for matched SDS-Plus
Switching an impact drill out of hammer mode to standard drilling mode is a collar-position and mechanical-engagement decision, not an electronic reset. The mode ring physically detaches the cam-and-rack (hammer) mechanism from the planetary gear train, restoring the slip-clutch torque limiter that
Immersion vibrator head eccentric bearing wear shows up as overheating, dropped RPM, and grease or oil at the seal. Field manuals point to lubrication loss, dry running, and contaminated seals as the dominant failure paths, and a 25-35 mm diameter head typically runs 9,000-12,000 VPM on its ball bea
ICC-ES AC133 (24) 2nd Edition, published April 2025, governs mechanical splice systems for steel reinforcing bars in U.S. concrete construction. It defines Types 1, 2, and 2HS (high-strain) splices with monotonic, cyclic, and residual-slip test stages referenced against ACI 318-19, Section 18.2.7.1
Self-climbing (hydraulic) formwork lifts the entire platform via hydraulic rams anchored to the previous pour, with no crane; crane-climbing systems rely on a tower crane for every jump. Self-climbs win on tall cores, limited-crane sites, and high-wind regions; crane-climbs remain cheaper for mid-ri
Hydraulic-drive and mechanical-gearbox ride-on power trowels split the slab-finishing market by power, feedback, and ownership cost. Mechanical units are cheaper and lighter; hydrostatic models use independent drive motors, eliminate belts and clutches, and run rotors up to 160 rpm for tighter FF/FL
Poker vibrators typically deliver peak vibration velocity of roughly 1.0 to 3.0 mm/s at the head, driven by eccentric weights spinning at 8,000 to 16,000 vpm across 25-100 mm head diameters. Selection hinges on matching head diameter to element thickness, not chasing the highest amplitude.
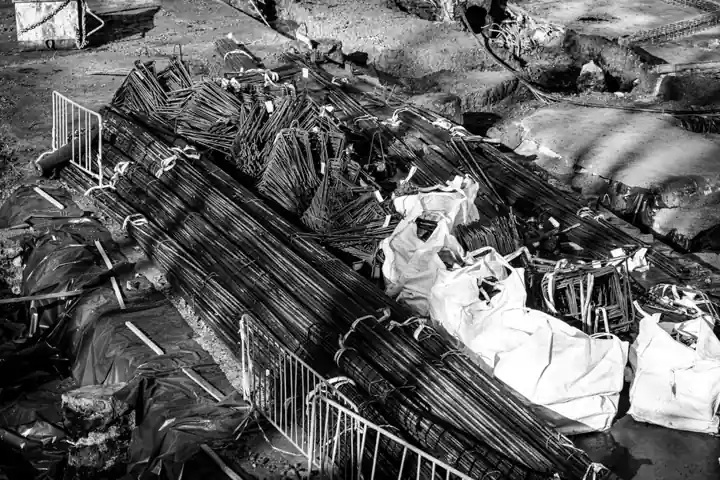
Mechanical couplers cut rebar use by up to 50% versus lap splices on congested or epoxy-coated joints, with the splice hardware adding roughly 0.2% to total structure cost. The rebar savings alone usually offset that premium on columns using #14+ bars.
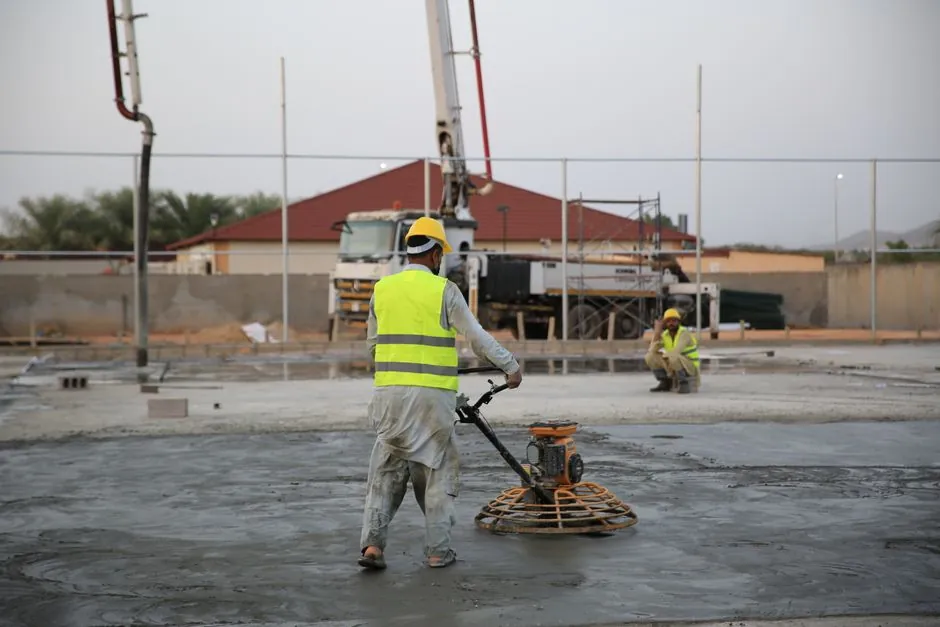
A 60 m3/hour pour needs 2 to 4 operators with poker vibrators running on a 6 to 10x-diameter insertion grid, sized 38 to 75 mm for typical slab and wall work. Most commonly, 3 to 4 pokers are deployed, with at least 1 hot spare for continuous flow.

Drawn arc stud welding typically uses 100 A per 1/16 in (≈1.59 mm) of stud diameter, roughly 63 A/mm, with weld times between 0.06 and 1.25 seconds for studs 1/4 in to 1 in (M6 to M24). Actual current varies with stud size, base metal thickness, and position.
On-site radius of action of a poker vibrator is verified by observing the bubble-escape zone around the inserted head, then setting insertion spacing at 1.0–1.5× that radius, with a common rule linking radius to roughly 10× head diameter (or 6–10× per spacing guidance).
Internal needle vibrators should be withdrawn at roughly 1 inch per second (≈25 mm/s), with each insertion held 5-15 seconds. Withdrawal rate, insertion spacing of 1.5× head radius, and frequency of 8,000-12,000 vpm govern consolidation quality per ACI 309R-05.
Concrete consolidation by vibration removes entrapped air by liquefying the fresh mix so bubbles rise and escape, with effective spacing of one head diameter per five inches of wall; under-vibration causes honeycombing while over-vibration causes segregation.
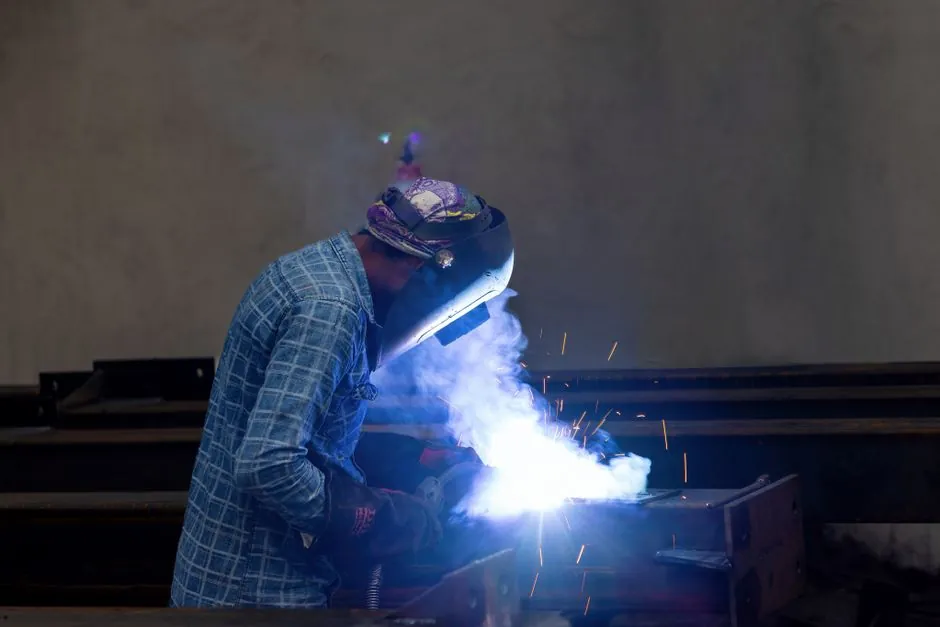
Arc force (also called dig or arc control) on a stick welder is a transient current boost triggered when arc voltage drops, typically below 19 V. Higher settings clear shorts and push the bead into open roots on E6010/XX10 electrodes, but the same surge tears E7018 globules apart and throws spatter;
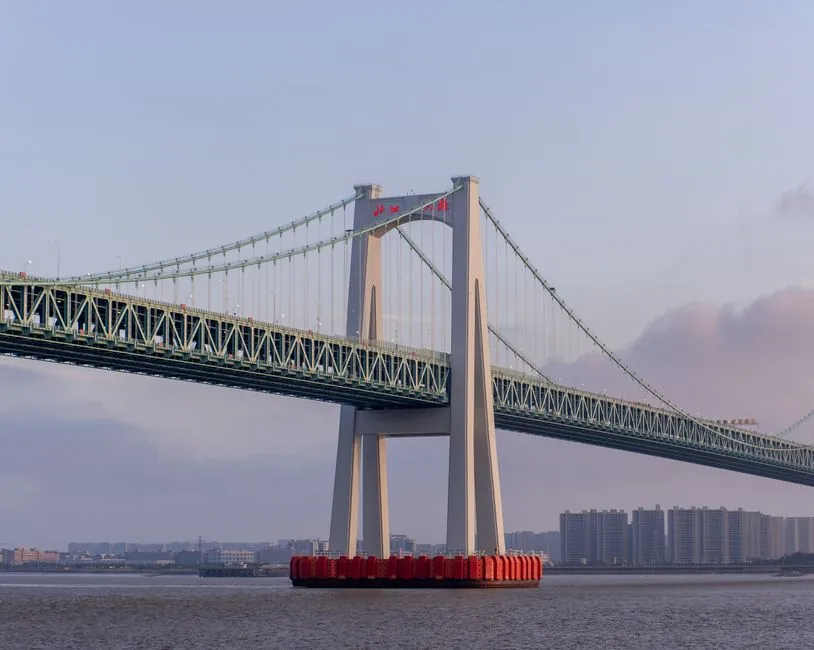
An underdeck suspended platform travels along a bridge girder by hanging from wire ropes or hangers anchored to the deck above, then shifting horizontally on rollers, wheeled bogies, or a dedicated under-bridge access carriage as work progresses.
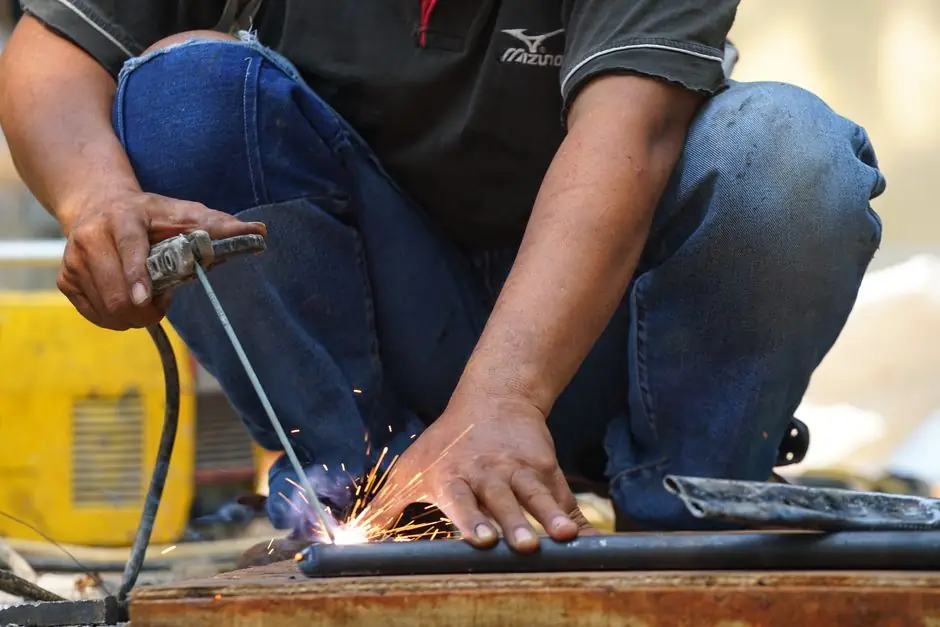
An arc welder strikes and holds an arc by forcing welding current across a sustained gap between electrode and base metal, typically at about 20 V for stick welding, with arc length setting voltage and current setting heat input. A constant-current supply keeps amperage steady as the operator varies
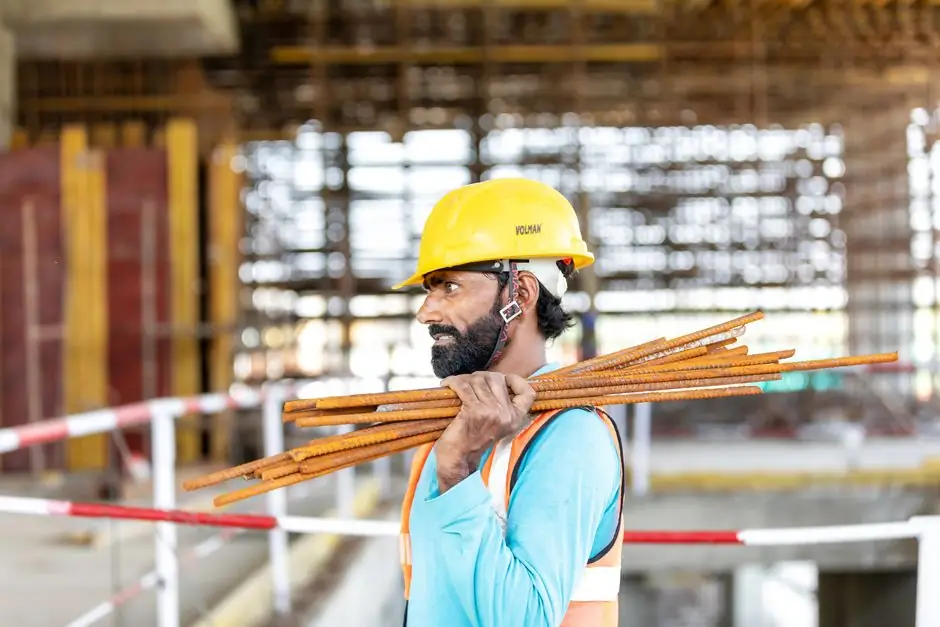
A bar bender reads a bar bending schedule (BBS) row by row, treating each line as one fabrication instruction: bar mark, diameter, shape code (BS 8666:2020 or IS 2502), cutting length in mm, and quantity. Operators cross-check shape codes against bending machine pin sets, then bend each bar to the s
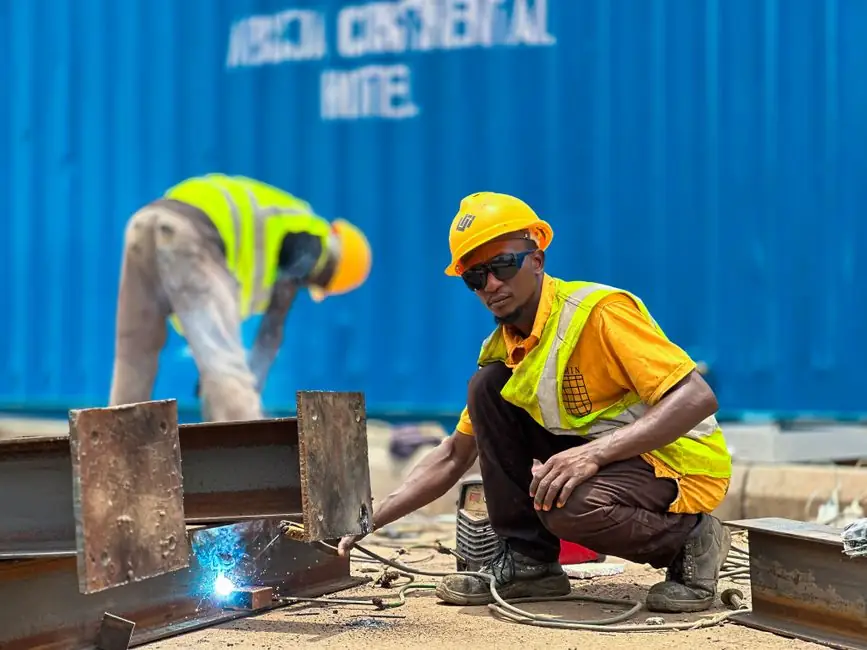
Drawn-arc stud welding can be performed in vertical and overhead positions on qualified CD studs with ferrule, using short weld times under 1 s and adjusted current/lift to hold the molten pool against gravity. The process is more tolerant of position than arc welding because the stud itself is plun
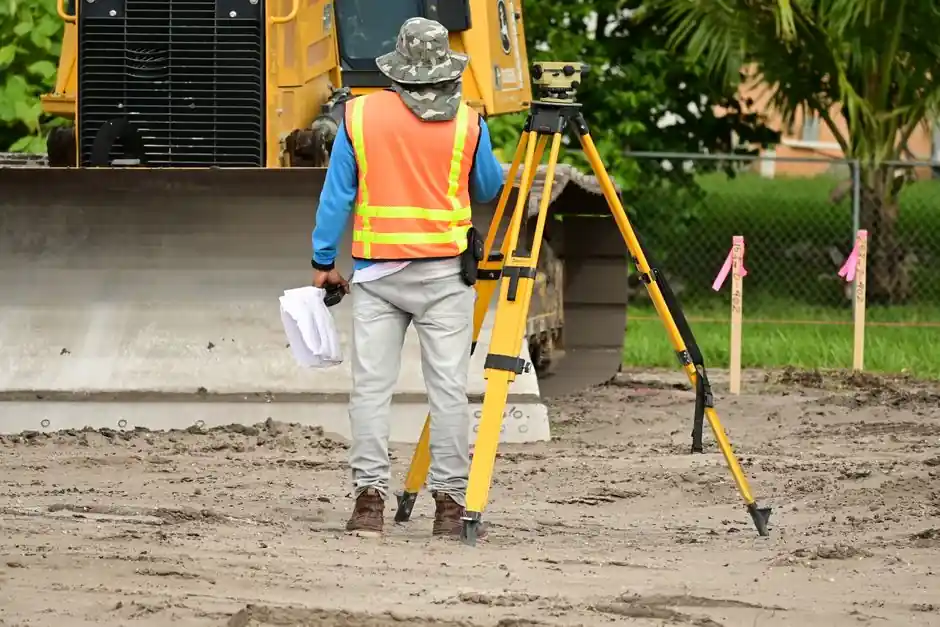
Set a laser level's slope function by calculating target gradient as a percentage, overriding the self-leveling compensator via the unit's grade or slope mode, then verifying the projected plane with a grade rod and detector at the far benchmark. Rotary grade lasers handle drainage 0.5–2% natively;
A 2% slope over 30 m of horizontal run produces a 0.60 m rise; read on a grade rod that is 0.60 m lower at the downhill end and break the run into sub-readings to keep every staff shot inside 0.30 m of level for sub-cm accuracy.
Match the aluminum ladder to the working height: add 7 to 10 ft of ladder length above the highest contact point for extension ladders, or use a stepladder rated for the standing level you need, per Werner, ALI, and Home Depot guidance.
Stud welding WPS qualification is driven by AWS B2.1/B2.1M and BS EN ISO 14555:2014, requiring documented current, time, polarity, lift, and plunge within tested ranges, with PQR verification via bend, tension, or torque tests.
GTAW and TIG are the same welding process: Gas Tungsten Arc Welding, with TIG as the informal shorthand. The American Welding Society uses GTAW, while "TIG" (tungsten inert gas) and "Heliarc" are common trade and regional labels for the identical non-consumable tungsten electrode, inert-shielded arc
For new precast and staged-build reinforcement splicing, grouted sleeve couplers win when bar rotation is impossible and field tolerance is critical, while threaded couplers win for compact, factory-prepared Type 2 splices on fixed-diameter bars. Both must satisfy ACI 318 mechanical-splice requireme
Forged top cups and ledger blades carry higher load and show more stable quality than pressed-steel cuplock cups, but pressed variants are widely used for lower-tier and non-shoring access. Selection depends on cup spec, material grade, weld pattern, and rated load path.
For internal concrete consolidation, flexible-shaft, motor-in-head, and pneumatic poker vibrators split the work: flex-shaft for low-cost general pours, motor-in-head for high-frequency noise-sensitive sites, pneumatic where no electricity is available. Match the head diameter (10-90 mm) to slump an

External mold vibrators for precast moulds typically deliver 2.9–60 kN centrifugal force (294–6,118 kgf) at 3,000–12,000 VPM, with high-frequency 6,000 VPM (100 Hz) units the most common for steel-mould compaction on box elements.

Encapsulated underdeck platforms integrate suspended scaffolding, full containment, and abrasive blasting into a single mobile envelope for bridge rehabilitation. Lead-paint encapsulation overcoat, RUST GRIP® encapsulation, and HP35-class under-bridge units (35 ft platform reach, 18 ft drop, 1,000 s

Dry-cut carbide metal saws run 1000-1500 rpm with replaceable toothed blades, while abrasive chop saws spin 3500-5000 rpm with $5 consumable discs. Choose carbide for clean, burr-free cuts and aluminum compatibility; choose abrasive for low-cost, high-speed rough cutting of steel stock.

Drawn arc stud welding runs 100-1500 ms at diameters from 2 to 25 mm with a ceramic ferrule or shielding gas, while short cycle (SC) drawn arc cuts the weld time to a maximum of 100 ms, drops minimum sheet thickness to 0.5 mm, and removes the ferrule up to 8 mm stud diameter. Both lift the stud to s

Drawn arc stud welding requires a 1/8 inch (3.2 mm) plunge depth past the ferrule and a lift height of 1/16 to 1/8 inch depending on stud diameter, with current 600 to 3000 A and weld time 100 to 1500 ms for full-penetration ferruled welds on 2 mm plus base material.

A concrete vibrator head does not rotate as a whole; an internal eccentric weight spins inside the steel housing, producing high-frequency oscillation that liquefies fresh concrete. The mechanism is best described as a rotating offset mass that creates orbital vibration, with typical influence radii

Dropping an automatic level can break the compensator suspension (mylar or metal ribbons) and stretch it, knocking the instrument out of calibration. Field checks after a fall are mandatory; severe impact generally requires compensator replacement, not field repair.

Self-climbing formwork uses hydraulic rams and does not need a tower crane to jump; crane-dependent and single-sided variants still do. Choose by structure type, height, and wind exposure, not by default.

DC current, specifically DCEP (electrode positive), is the standard choice for deep-penetration arc welding on steel; AC provides deep penetration mainly with cellulosic electrodes like E6011 and in aluminum TIG oxide cleaning. Selection depends on electrode type, base metal, and position.

Yes. U.S. 29 CFR 1910.66(f)(5) requires every single point suspended working platform to carry an independent secondary wire rope suspension system, and EN 1808 applies the same logic to two-point platforms via a secondary brake on the hoist. The secondary line or device is non-substitutable: it mus

Cut accuracy on steel bar is determined less by the saw type than by the machine features that control deflection, length repeatability, and end quality. Rigid saw heads, CNC servo positioning, and thin-kerf abrasive wheels routinely hold ±0.001–0.008 in tolerances on bar stock.

Abrasive-wheel chop saws cut 5-10x faster than cold saws but generate friction heat, sparks, and burrs; cold saws (20-150 RPM, HSS or carbide-tipped blades) deliver burr-free, metallurgically clean cuts and lower per-cut cost. Pick the cold saw for steel, stainless, and aluminum when tolerance and f

For cuplock vertical standard stacking, a 38 mm OD spigot joint pin is the dominant spec across both square and round profiles, matched to 48.3 mm scaffold tubes and produced in 150-300 mm lengths in mild or high-strength steel. Square spigots win on alignment stability and heavy slab work, while ro

Cuplock scaffolding vertical standards use a fixed 500 mm cup spacing as the industry-standard node interval, welded at half-metre centres on a 48.3 mm OD steel tube. This 0.5 m grid sets the lift height and limits each node to four horizontal connections, driving every bay and bracing decision on t

Cuplock scaffolding joins vertical standards and horizontal ledgers through a forged ledger blade that drops into a fixed lower cup, then is locked by a sliding upper cup struck with a hammer. This cup-and-blade node accepts up to four ledgers per joint, is welded at 0.5 m vertical intervals, and fo

Constant-speed electronics on corded percussion drills hold a chosen no-load RPM within a tight band as load rises, achieved by a feedback loop that boosts armature current on stall. The Metabo BEV 1300-2 is a current production 1,300 W example with a two-speed gearbox and constant electronics, and

Constant current (CC) and constant voltage (CV) arc welding power sources differ in whether they hold amperage or voltage stable as arc length changes, with CC suiting manual SMAW/TIG and CV suiting self-regulating MIG/MAG/FCAW wire processes. A CC machine typically limits current swing to roughly ±

Eccentric concrete vibrator heads pair an internal rotating shaft with a flexible drive core, available in 29-65mm head diameters and 4-6m shaft lengths. Selection pivots on head size, frequency (200-280Hz), and the motor-to-head coupling type, with regional coupling standards shaping spare-parts so

Concrete vibrator radius of action shrinks from roughly 1.5-2 ft in stiff, low-slump mixes to a few inches in flowing, high-slump concrete, so head diameter, frequency, and amplitude must be matched to workability, not just member thickness.
The compensator check button on an automatic level is a push-and-release test that confirms the pendulum-style compensator is freely suspended and damping-damped; a clean response indicates the line of sight is self-leveling, a sluggish or sticky response flags the instrument for service.

Climbing (jump) formwork and slipform both self-climb on the previously cast concrete, but jumpform pours in discrete lifts of roughly 2 m while slipform extrudes continuously at about 300 mm/hour, so the choice hinges on geometry, height and joint visibility. Core walls above 7-10 storeys, tapered

Climbing (jump) formwork typically cycles 3 to 5 days per floor on high-rise cores, limited by concrete cure rather than the 30 to 60 minute self-climb itself. Self-climbing hydraulic systems outperform crane-climbed setups when wind, geometry changes, or crane availability restrict lifting windows.

Circular saw blade pricing in the U.S. for 2026 clusters between $25 and $90 per blade for 7-1/4″ carbide-tipped models, with tooth count and carbide grade acting as the dominant cost drivers alongside diameter and coating. Buyers can drop effective per-cut cost by 30-50% through 5-pack bulk buying

High-speed steel raw material drives 60–70% of circular saw plant operating cost, while finished-tool retail prices are governed by motor winding, gear-train machining, and the share of die-cast subassemblies in the bill of materials.

The circular bubble on an automatic level must be centred using the three foot screws before the internal compensator takes over; field adjustment is a 180-degree reversal test with the bubble, corrected by half-error at the adjusting screws until the bubble stays centred at 90-degree and 360-degree

For percussion drilling in concrete and brick, specify quad-tip (cross/four-cutter) carbide SDS bits for abrasive or rebar-likely mixes, and stick with two-cutter chisel-tip bits for brick, block, and light concrete to control cost. The 1/8"–1/2" range covers 90% of anchor and through-hole work.

CD stud welding splits into contact and gap methods: contact sits the stud on the workpiece, vaporizes the tip, and completes the weld in roughly 3 ms; gap lifts the stud to a defined standoff for higher plunge speed and welds in about 1 ms, which is what makes aluminum and brass practical without s

Cast-in anchor plates paired with climbing cones transfer higher tensile loads per cycle and dominate on high-rise, dam, and bridge pours, while post-installed climbing cone anchors win on retrofit and repair scopes where the concrete is already cured. The decision pivots on pour-stage access, reusa

Capital cost for a carbide circular saw blade brazing and grinding line ranges from roughly USD 18,000 for a manual ZSC solder-tape station to over USD 60,000 per automated CNC brazing cell, with induction-heated models such as the WEHO MZ079 (120–790 mm capacity, 6.5 kW total) and YUANDA ZDH-series

Capacitor discharge (CD) stud welding suits thin sheet from 0.5 mm and stud diameters M3 to M10 at ≤3 ms weld time, while drawn arc (DA) covers 2-25 mm studs on ≥2 mm plate at 100-1500 ms with ceramic ferrules. Choose CD for clean, automated, thin-gauge work; pick DA for structural, large-diameter,

A hammer drill in hammer mode will fracture granite tiles or thin countertop sections; the safe, repeatable method is a rotary drill (or hammer drill with hammer function OFF) running a diamond-tipped bit or diamond core hole saw at low RPM with continuous water cooling, at roughly 600-1,200 RPM for

A rotary laser level plus grade rod and receiver can measure the slope of an existing surface by reading elevation differences at two points and dividing by horizontal run, typically expressed as a percentage. Manual self-leveling units cover 2-point checks; dual-axis slope models handle longer runs

BS 8597:2015 is the BSI standard that defines requirements and test methods for steel reinforcement couplers used to mechanically splice reinforcing bars; a revision is in active development with publication scheduled for 30 November 2026.

Air impact wrench blow rate (IPM/BPM) typically ranges 1,000 to 1,500 blows per minute on 1/2-inch pneumatic models, with twin-hammer designs driving faster impact cycles than single-hammer units. Free speed, BPM, and CFM must be matched to compressor capacity at 90 PSI minimum to avoid stall.

AWS C5.4-93, the recommended practices for stud welding, has been formally withdrawn without a published replacement, leaving engineers relying on AWS D1.1 and ISO 14555 for procedure qualification. The 1993 document still defines the core method, base-metal thickness, and troubleshooting matrix for

Avalanche photodiode (APD) receivers deliver 6 to 8 dB sensitivity gain over PIN photodiodes in laser ranging, with Si-APDs covering 400 to 1100 nm (peak ~900 nm) and InGaAs/InP APDs extending to 1700 nm for eye-safe and long-range designs.

A rotary laser level with slope mode is a precision instrument that projects a beam at a user-defined angle, typically 0° to 25°, by overriding its self-leveling mechanism on one or both axes. Dual-axis models are required for compound grades such as ramp-and-cross-fall, while single-axis units hand

Auto levels read a graduated staff by eye through an optical compensator; digital levels image a barcode staff and compute the height electronically, cutting reading error and roughly halving field time on repetitive levelling runs.

An automatic level relies on a centered circular (bull's-eye) bubble to feed the internal compensator, with a tubular vial reserved for fine adjustment on dumpy or digital levels; the two designs are not interchangeable at the coarse-stage setup. A 20-second tubular vial reads 9.7 mm of elevation er

Automatic level recalibration costs range from $95 for a basic tune-up to $240+ for digital and optical tooling levels, with most survey shops charging a $110 inspection fee before issuing a fixed repair quote. Total cost of ownership over a 5-7 year service life is dominated by the recalibration in

Automatic level collimation error that exceeds roughly 0.05 ft/100 ft (6 mm per 30 m) on a two-peg test is the working threshold for scheduling recalibration before field accuracy drifts out of spec; tighter work demands 0.02 ft/100 ft, and an annual or semiannual accredited lab check paired with mo

An automatic level is an optical surveying instrument that uses a gravity-suspended compensator to maintain a true horizontal line of sight, replacing manual vial adjustment with self-levelling. Typical contractor-grade units deliver 20x to 32x magnification, ±1.5 mm/km double-run accuracy, and a wo

For an automatic (optical) level, stepping the objective clear aperture from 40 mm to 45 mm lifts geometric light-gathering area by roughly 27% and, more importantly, raises image brightness on the reticle plane by an even larger factor once magnification is held constant. The real-world gain is ima

32X magnification auto levels from Spectra Precision, K-LEVEL, David White, GeoMax and Doyen now deliver 100-120 m working range and 1.0-2.0 mm/km leveling accuracy for builders and surveyors.

Automatic level compensators self-level within roughly ±10 to ±30 arc-minutes of vertical-axis tilt; outside that window the pendulum or prism assembly hits its mechanical stops, the line of sight is no longer corrected, and the instrument throws an out-of-range error rather than a graded reading.

An automatic level's compensator holds the line of sight to a horizontal reference within roughly ±0.5 arc seconds on premium models, equating to about ±1.5 mm at 76 m or ±1.6 mm at 30 m; mid-range optical auto levels deliver ±1.5 mm at 30 m, while 20-30 arc-second vial instruments are confined to r

ASTM A1034/A1034M-24 is the current specification for mechanical splices on steel reinforcing bars, with the parallel -23 test methods document still active as of January 2024. Scope covers any splice type, any rebar grade, coated or uncoated, with results reported in SI or inch-pound units.

Three-phase arc welding power sources deliver smoother arcs and higher duty cycles for industrial work, while single-phase units fit mobile and small-shop use. Match the input phase to your facility's service, output current, and duty-cycle demand.

Welding transformer rating for continuous production welding is set by secondary current capacity at a defined duty cycle, typically 400-600 A on the 415 V primary side per SAIL IPSS 1-07-001-95. For multi-station plants, the 60% duty cycle rating is the spec that matters, not nameplate kVA.

For pipe root passes, TIG (GTAW) and Stick (SMAW) dominate field and shop practice, with TIG specified for stainless, aluminum, and code-critical joints, and Stick chosen for portable, outdoor, multi-pass fill work. Selection hinges on base metal, weld position, code requirements, and field conditio

Arc welding machine open-circuit voltage (OCV) typically sits in the 50-80 V range, with AC arc welding specified at 50-90 V and reputable inverter MMA/stick welders delivering 50 V or more for reliable arc striking.

An arc welding machine rated at 200 amps with an 80% duty cycle can sustain arc-on time for 8 minutes of every 10-minute cycle under 40°C ambient conditions, per the Amico ARC-200 spec sheet. At 60% duty cycle the same machine delivers 6 minutes of welding per 10-minute window; at 30% it drops

Arc welding runs on either AC or DC power, with the choice dictated by process and base metal: DC (DCEN or DCEP) drives most SMAW, GMAW and FCAW, while AC remains the default for GTAW on aluminium and for arc-blow control. Practical selection hinges on penetration, heat balance and magnetic-field co
Delivering 200 A from a single-phase arc welder requires a 50 A breaker at 208-230 V primary, drawing roughly 6,000-10,000 W on inverter units and up to 44 kW theoretical input for legacy transformer MIG sets, per published sizing guidance.

Shielded metal arc welding (SMAW), the formal name behind "stick welding," uses a flux-coated consumable electrode fed by AC or DC constant-current power to deposit filler metal under a self-generated shielding gas. It welds carbon steel, stainless steel, cast iron, nickel and copper alloys in field

TIG welding is the trade name for gas tungsten arc welding (GTAW), an arc process using a non-consumable tungsten electrode and an inert shielding gas; the American Welding Society term GTAW and the older Heliarc name both refer to the same process.

Angle grinder disc diameter sets the no-load speed band: 115 mm discs typically spin at 11,000 RPM, while 230 mm discs run near 6,000 RPM. The binding limit is the 80 m/s maximum peripheral speed printed on every certified abrasive wheel.

For 115mm vs 125mm vs 230mm angle grinders, the 125mm hits the best capacity-to-handling balance for general metal work, 115mm is the precision and one-handed choice, and 230mm is reserved for heavy stock over 6mm and concrete cutting. All three share a 22.2mm bore and M14 spindle, so only the outer

Aluminum ladder duty ratings are defined by ANSI/ALI A14 standards across five classes: Type IAA 375 lb, Type IA 300 lb, Type I 250 lb, Type II 225 lb, and Type III 200 lb. Selection hinges on total load (climber plus clothing, PPE, tools, supplies) and on electrical-hazard exposure.

Aluminum extension ladders require at least 3 ft (0.91 m) section overlap for ladders up to 36 ft and 4 ft (1.22 m) for 40 ft and longer, with some sources citing up to 5 ft on the longest units. Working height should be planned 7 to 10 ft longer than the highest contact point because overlap and st

Twin hammer and single hammer air impact wrenches differ in mechanism, power density, and best-fit use: twin hammer delivers higher free-speed RPM and instant torque for hard joints, while single hammer gives one stronger blow per revolution for soft joints.

ACI 309R guidance sets vibrator insertion spacing at 1.5 times the radius of influence (or radius of action) to ensure overlapping consolidation zones, per ACI 309R-05 Table 5.1 and field practice guidance.

600 W percussion drills cover light masonry and 13 mm metal work, while 1100 W units reach 16 mm in steel, 40 mm in timber, and 22 mm in concrete with 50-60% motor efficiency, so spec by output watts and chuck capacity, not input watts.

For interior fit-out, a 3x360-degree line laser is the better buy when layout spans multiple walls, ceilings, and floors, while a cross-line laser remains the cost-effective pick for single-wall, short-range trim work. Tested 2026 models from Huepar, DeWalt, Bosch, and Klein show accuracy ranging fr

A 3/8-inch stubby air impact wrench in the 450 to 710 ft-lbs class is the right pick for engine bay work where fastener recess depth, not raw power, is the limiting factor. Pick pneumatic for sustained shop use, battery (M12 FUEL) for mobile calls, and verify length-under-4.8-inch for transmission t

For heavy truck tire work, a 3/4 inch drive air impact wrench is the practical choice; 1 inch drive delivers more torque but adds weight, larger sockets, and higher air consumption. Match drive size to fastener size and lug-nut torque, not to perceived power.

Aluminum ladders fail through five dominant modes: axial-restrained buckling, rail/rung cracking, hardware loosening, electrical conduction in energized environments, and foot slip on unstable ground. Prevention pairs pre-shift inspection, the 4:1 set-up rule, non-conductive substitution near live c

Wet-mix shotcrete machines on bridge repair and new-build sites require nozzle-velocity checks, conveyor/auger cleaning, and accelerator dosing calibration every 50-100 operating hours to keep rebound under 10% and maintain ACI 506 nozzle pressure near 100 psi.

AWS D1.1 requires 100% visual inspection of every stud weld on structural steel work, with bend testing triggered by any incomplete 360° flash ring. A passing weld shows a complete continuous fillet, centered plunge, and no undercut or porosity; a failed weld is removed and replaced, not repaired.

Stud welder commissioning on a structural project starts with AWS D1.1 daily operator/equipment qualification: a 2-stud test per shift, 100% visual flash-ring check, and a 30° or 60° bend test, all traceable to ISO 14555 and the project WPS. Visual evidence is necessary but never sufficient on its o

Stud welding safety requires five layered controls: ANSI-rated PPE, a 35-foot combustible clearance, forced ventilation, dry insulated circuits, and operator training against OSHA 1910/1926 Subpart Q and J.

Stud welding joins a metal fastener to a base plate through a controlled electric arc, requiring no filler material and completing the fusion in roughly a tenth of a second per cycle. It is split into two main industrial variants: drawn-arc stud welding and capacitor-discharge (CD) stud welding, wit

Sanding-belt failures cluster into seven recurring modes (loading, glazing, tracking, stretch, tearing, burning, and premature wear) traceable to grain choice, belt speed in SFPM, contact pressure, and backing weight. Prevention is a matching exercise, not a replacement exercise.

For plumbing rough-in and drain-slope work, specify a self-leveling line or point-to-line laser with ±1/8 in accuracy at 30 ft, green beam for interior visibility, IP54+ rating, and dual plumb/horizontal beams at 90°. Rotary lasers only become necessary for outdoor sewer runs beyond 150 ft.

Electrical preventive maintenance that pairs scheduled visual, thermal, and electrical tests with de-energized cleaning prevents over two-thirds of distribution failures and cuts failure rate 3x vs unscheduled equipment, per Hartford Steam Boiler EPM guidance. Core tasks: infrared thermography on en

Fiber laser welder installation boils down to eight sequenced checks: stable dry site, matched mains supply, argon shielding at >0.2 MPa / >15 L/min, distilled-water cooling, wire-feeder setup, external emergency stop, parameter test welds, then production. Skipping the gas-pressure or water-quality

Industrial sander service life spans 5-15 years on the tool body, while consumable lifespans vary: sanding discs last 15 minutes to several hours, belts 5-15 hours, and pads 6-12 months, depending on abrasive type, workload, and maintenance.

A sander's testing and commissioning procedure spans electrical safety pre-checks, mechanical pre-start inspection, and, on HVAC trade sanders like NEBB TAB firms, formal balancing sign-off. A pre-use 100% test on safety and operating rules, a UK 3-pin plug and grounding verification, and dust-extra
A total station installs in three verifiable phases — tripod/tribrach leveling, on-site calibration, and target/reflector lock — with prismless ranges of 300–500 m and angle accuracy from 2″ to 5″ governing acceptance.

For food and beverage plants and commercial kitchens, a laser distance meter works when it carries an IP54+ rating, runs class 2 red laser under 1 mW, and survives routine wash-down; top picks are Fluke 417D (131 ft / 40 m), Leica Disto D5 (660 ft / 200 m) and Laserliner LaserRange-Master T3.

Marble cutters are handheld 1200 W class angle-grinder style tools with 11000–13000 RPM no-load speed, 2.5–3.5 kg weight, and 4–4.5 inch diamond or abrasive blades, usable on steel, stone, tile, and concrete with the right disc. For steel construction they work for thin sheet and rebar trim cuts onl

Concrete work demands a power mixer sized to batch volume and power-source constraints: 60-190 L electric units for site work, 250 L+ combustion units for daily pours, with 700 W minimum and 500-1500 W typical for 220 V single-phase models.

Electroslag pressure welding (ESW) ties rebar splices in 1-3 seconds per joint, but the 5-10 year TCO is dominated by flux, water-cooled copper mould consumption, and joint-rejection rework, not the machine's purchase price. Specifying for column-dense high-rises on a 30-second per splice budget is

Circular saws for bridge construction are sized by blade diameter 250-400 mm with TCT teeth, kerf 2.5-4.0 mm, and max RPM 3,800-4,500; concrete cutting demands diamond blades rated for 35-65 MPa aggregate and water suppression, not TCT wood blades.
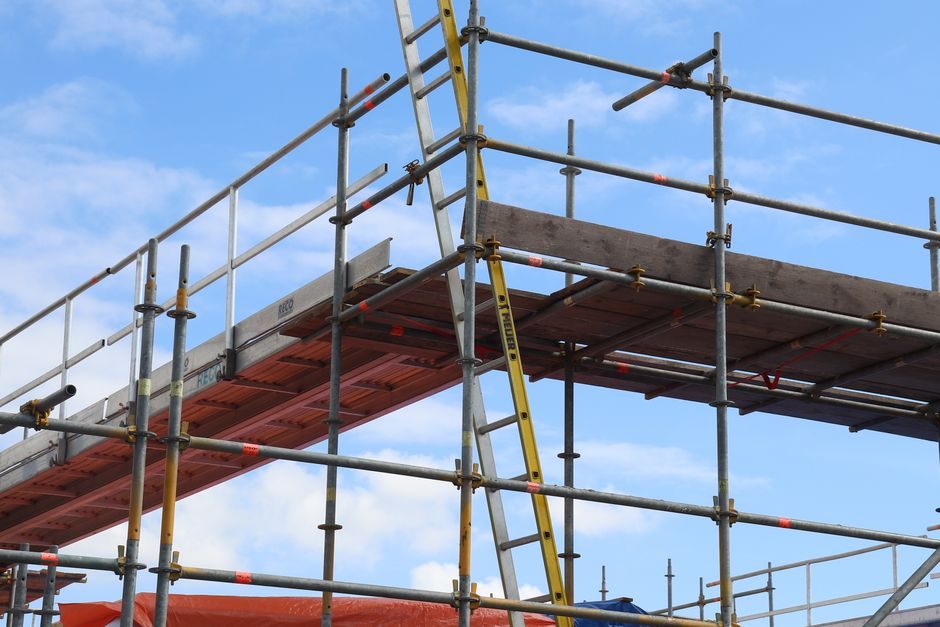
Aluminum ladder installation hinges on matching the ladder class to the task, verifying the 150 kg rated load, setting the correct 75° lean angle, and confirming stabilizer-foot contact before climb. Skip aluminum for live electrical work above 1 kV unless the alloy is certified non-conductive for t

Pneumatic nail gun supply is concentrated in Zhejiang and Guangdong, China, with framing/finishing/coil/roofing variants; mid-range 2026 export FOB bands run US$31–36/piece MOQ 1, with 13 OEMs and 37 SKUs tracked on DirectIndustry.

A stud welder's true lifecycle cost over a 10–20 year service window is dominated by energy, consumables, downtime and weld-quality rejects, not the inverter price tag. A 5-axis TCO model — acquisition, energy, consumables, maintenance, downtime — lets buyers compare capacitor-discharge, drawn-arc a

Gravity roller flow racks move loaded units from the back to the picking face on a shallow incline, enforcing FIFO rotation without motors or controls. They are one of several pallet rack families selected by throughput, density, and stock-rotation needs rather than by a single universal principle.

Rebar straightener maintenance on plumbing jobs hinges on three things: keeping the straightener's roller geometry true, isolating it from water-line vibration, and never running deformed coils through the unit. Use this guide to keep your rebar straightener cutting clean bends without contaminating

Power mixer spare parts split into four wear tiers, drive-train (gears, worm pinion), fluid-contact (impellers, seals, bowls), structural (housings, guards), and consumables (lubricant, gaskets). Spec the right part by matching model number, batch volume, and duty cycle. Reference the power mixer en

A mezzanine platform is an intermediate free-standing floor built inside an existing building to add usable area between the ground and the roof. The dominant industrial types — rack-supported, steel-structure, and office/retail — differ on load class, column grid, and integration with adjacent stor
For landscaping, a portable electric or small gas power mixer in the 1.5–6.0 cu ft drum class fits most residential and light-commercial jobs; drum tilt or paddle type is selected by aggregate size and slump target, with OSHA silica Rule coverage on every site.

Stud welders for demolition work are drawn-arc systems sized for large-diameter studs, typically 3/8 to 1 inch, paired with portable power units and portable demolition hammer tooling. Choose drawn-arc over CD for thick base metal, and check stud alloy limits above 0.25% carbon.

Cut-off machines for concrete work split into three classes: 110-125 mm handheld electrics (around 1,400 W), 355 mm portable steel/stone cutters (2,200 W class, 3,800 rpm), and 762 mm foundry swing-frame saws (30 HP, 14,200 SFPM). Pick by blade diameter, motor power, and whether the cut is handheld

MIG welding machines and arc welding machines overlap on ISO 4063 process codes 131/135/111 but differ on consumable electrode, shielding gas, duty cycle, and integration. Spec MIG for high-deposition manual/robotic steel work; specify MMA/stick arc for field repair and outdoor sites without gas sup

Electric rebar cutters for masonry sites cover 10-42 mm bar diameters, with 110 V portable hydraulic units (Fascut FC-800) handling up to 1" (#8) grade 60 rebar and 180 lb two-person carry combos (FS-600) covering #6 grade 60. Match machine capacity to the largest bar on site, verify blade SKU match
Plasma cutter prices span US$260 handheld inverter units to US$18,000 gantry CNC tables; total cost of ownership is driven by cutting thickness, automation class, and consumable lifetime, with steel severing capacity ranging from 25 mm inverter class to 100 mm CNC gantry class.
Marble cutter selection for landscaping is dominated by 110-125 mm handheld angle grinders at 1200-1400 W with continuous-rim diamond blades, sized to paving stone and coping stock. Hire/contractor crews can run corded 125 mm tools; finer detail on statuary and water-feature trim shifts to a cordles
A handheld marble cutter fitted with a diamond blade rated for cured concrete is the practical choice for short-run scoring and chase cutting on slab work; for walls and slabs thicker than ~100 mm, a concrete groove cutter on a walk-behind platform delivers cleaner, deeper channels at lower per-metr

Henan-based cluster of 5+ Chinese shotcrete machine makers commands global B2B listings as of July 2026, with wet-mix robotic arms like Normet-class units quoted at USD 250,000-350,000 FOB and small dry-mix sprayers starting at USD 5,299 per set.

For landscaping, the concrete groove cutter you pick depends on whether you are scoring control joints in fresh slabs, sawing expansion joints in cured pavement, or trenching for landscape lighting and irrigation: 125-180 mm diamond blades, 3-9 kW petrol power and 4,800-7,200 rpm blade speed cover m

For demolition work, a self-leveling rotary laser with a 1,000+ ft receiver range and IP67 rating is the practical baseline; a laser level selection pivots on range, IP rating, and beam color rather than interior features.
Pneumatic nail gun entry-level FOB pricing sits at US$31-36/piece at 1-piece MOQ from Liaoning suppliers, mid-band insulation nailers land at US$85-90/piece at 10-piece MOQ, and IMCOINSA 0A6 series framing tools anchor the upper spec tier for wood framing in 2026 sourcing catalogs.
For plumbing-install jobs using threaded rebar, a 380 V, 3–6 kW CE-marked automatic rebar threading machine with tangential chasers and 100–300 mm thread length is the typical shop-floor package, with 40CR or 45# carbon steel couplers paired to it.

Power mixer selection for masonry hinges on matching auger throughput, batch volume, and dust-mitigation design to project size — paddle mixers need 3–5 min cycles per ASTM C270, while SPEC MIX PA4000 power augers deliver preblended mortar continuously for crews of any size.
For masonry under 13 mm in concrete and brick, a 500-700 W corded impact drill with a keyed or keyless 13 mm chuck and mechanical impact mode matches duty; for repeated 16-25 mm holes in cured concrete or for production volume, step up to an SDS-Plus rotary hammer instead.

For bridge construction, a marble cutter is selected as a bridge disc saw with diamond blade and high-speed cutting for slabs over 10 mm, paired with steelwork-fabrication methods compliant with BS EN 1090-2. Match power class to kerf depth, blade diameter to slab thickness, and wet-cutting dust con

Plasma cutters do not cut masonry: the plasma jet only cuts electrically conductive metals, so stone, brick, and concrete require a dedicated masonry cutting tool. For rebar or mesh embedded in masonry, a 60-100A plasma system handles 3/8-1 in steel clean cuts at 60-90 PSI and 4-8 CFM.

Plumbing installation on concrete slabs typically uses a 12-20 inch single-disc floor grinder with diamond-segment tooling, paired with a HEPA vacuum for dust capture; HP and head configuration drive fit. Final selection depends on slab hardness, removal depth, and whether a separate coring step is
Angle grinder installation hinges on a spindle-lock plus anti-lock flange pair, with abrasive disc match, guard set-point and PPE checked before mains or battery connection. The procedure below maps disc, guard and accessory change-out for 100/115/125 mm class machines.
Cut-off machines for industrial buyers split into handheld abrasive saws (2000–2200 W, 355 mm wheel, ~3800 rpm no-load) and larger benchtop/CNC abrasive cutters, with 2026 sourcing dominated by Chinese OEM models such as OUDERLI J1G-ODL-MT240 at MOQ 300 units and 30–45 day delivery.
Demolition hammers deliver 30–60 J single-stroke impact energy and 1000–2000 bpm for breaking concrete, asphalt and masonry, with a demolition hammer trade-off in vibration, dust load and operator fatigue versus lighter rotary hammer options.
Spot welding and arc welding serve different jobs: spot welders deliver high current through copper electrodes for fast, localized resistance joints (e.g. 20-32 kW Tecna/TECHNAX units), while arc welders use a consumable electrode arc for versatile structural joints (e.g. AC/DC inverter MMA

Plumbing-installation rebar cutting in 2026-08 hinges on matching a portable 10-32 mm electric or hydraulic rebar cutter to the bar grade (Grade 40/60), trench width, and the need for rust-free, square burr-free cuts that keep threaded sleeve and lap-splice tolerances inside ACI 318 Chapter 25 limit
Upset-forging parallel-thread couplers sized 12-50 mm dominate interior-finishing rebar splicing, with ISO 15835 category B/F/S certification and tensile capacity above 700 MPa the main engineering gates. Selection turns on bar diameter, congestion, and code class rather than price alone.

A rebar straightener inspection checklist for site and shop use in September 2026 must validate five machine subsystems (mechanical, electrical, hydraulic, straightness-output, and safety) plus material traceability. Acceptance criteria include ≤3 mm/m deviation on straightened bar, visible roll-con

A sander removes material by driving an abrasive medium against a workpiece, with the operating principle set by abrasive geometry: orbital pads oscillate in small ellipses, rotary discs spin on a fixed axis, and belt machines run a continuous abrasive loop over two motor-driven drums. Selection tur

Power mixer failures concentrate at the seal, shaft, bearing, gearbox, and impeller, with gearbox problems driving roughly 45% of incidents and recurring faults accounting for about 73% of all food-plant mixer breakdowns. Prevention hinges on lubricant analysis, vibration trending, seal-face inspect

A hose reel stores, dispenses, and retracts a flexible hose on a wound drum driven by spring, hand-crank, or motor. Operating principles differ by drive type, with fire hose reels using constant pressure water supply and manual nozzle control.

Power mixer inspection rests on four cadence tiers: pre-shift 12-point safety and contamination checks (8-12 min), weekly structural and lubrication walks, monthly impeller/seal/shaft audits, and full annual tear-downs. Seal failures drive 47% of contamination events; daily documented checks catch 7
Industrial power mixers in the 0.55–75 kW band typically reach end-of-life at 7–12 years under three-shift duty, with replacement driven by bearing failure, seal degradation, gearbox wear, and ATEX/IEC 60079 re-certification gaps rather than motor burnout alone. Plan a 30,000–40,000 operating-hour s

Construction stud welding maintenance on concrete anchor and shear-connector work pivots on three wear parts: the chuck/tip, the contactor, and the DC bus capacitor bank, with daily cable checks and 12-month OEM servicing extending gun life past 15 years on drawn-arc rigs.

Power mixer safety hinges on lockout/tagout of the power source, EN 62841 hand-arm vibration compliance below 2.5 m/s², and ATEX/IEC 60079 zoning for any installation near solvent or dust hazards.

Interior finishing laser levels last longest when operators combine daily lens cleaning, scheduled 180-degree calibration checks, dry padded-case storage, and proactive battery management, with concrete screed-class machines needing hydraulic and lubrication routines on top.

Demolition hammer failures cluster into four preventable modes: impact-performance loss, mechanical wear/seizure, dust evacuation faults, and seal/handle vibration breakdown. Carbon-brush wear, lubrication starvation, and bit mismatching cause most field downtime across 1500-2000 W handheld and 60-1

For bridge construction in 2026, handheld laser distance meters typically span 0.05–250 m with ±1–3 mm accuracy and IP54–IP65 sealing, while fixed bridge-deflection laser sensors reach 100 m (500 m with reflector) at ±1–5 mm with 10–250 Hz update.

For interior finishing work, specify 6061-T6 aluminum ladders under CSI 05 51 33, with ASTM B308/B308M rail profiles, AWS D1.2 welding, OSHA 1910.23 rung spacing of 10–14 in, 16 in clear width, and a 300 lb minimum live load. These criteria match mill-finish fixed access ladder offerings and let any

A demolition hammer pre-use inspection runs 7 to 10 grouped checks: housing, power source, controls, impact mechanism, bit condition, vibration isolation, and lubrication, with bits and anti-vibration mounts being the most common replace-on-site items.

A demolition hammer's service life is governed by housing material, hammer-mechanism size, lubrication discipline, and operator duty cycle, with magnesium-bodied SDS-MAX models typically outlasting plastic-housed light-duty units. Replacement decisions hinge on three triggers: carbon-brush wear, bea

Demolition hammer commissioning is a five-stage field procedure: pre-power inspection, no-load run, bit seating, loaded impact test, and dust/PPE verification. 80V cordless models add battery management; electric mains units require IR and ground continuity checks per standard practice.

Demolition hammer safety requires three layers: OSHA 1926.300 tool-condition compliance, APF 10 respiratory protection when silica dust exceeds trigger thresholds, and 90-degree perpendicular tool engagement. OSHA 1926.1153 mandates wet-method or VDCS dust controls on every concrete-breaking task.

Rebar cutter maintenance on bridge projects is dominated by four recurring tasks: hydraulic oil and seal checks, blade/shear life tracking (40,000–80,000 cuts at 32–40 mm), hydraulic hose inspection, and strict adherence to clamping and PPE protocols. Hydraulic electric units are the practical defau

Pneumatic nail guns used in HVAC duct and insulation fastening work best when fed with air-tool oil (not ATF, motor oil, or acetone), kept above 32°F, and run at the compressor's 70–120 psi range. White lithium grease is the correct choice for metal contact points, while high pressure above 120 psi

Marble cutter fleets fail in three predictable ways: blade segment loss from overheating or material mismatch, motor brush wear from stall, and bearing failure from dust ingestion. Prevention hinges on matching the disc to the substrate, keeping cooling vents clear, and enforcing a 30 mA RCD on any

A marble cutter draws on four consumable families (diamond blades, suction/vacuum handling, CNC spindle and PCD tooling, and small switch/handle/guard spares) stocked across OEM, agent and aftermarket channels, with parts priced from about $1.35 for a thumb screw to $46.92 for a replacement handle.

A marble cutter inspection checklist combines pre-cut slab approval (shade, veining, fissures, ±2-3 mm thickness, 45° finish check) with machine readiness (blade condition, water feed, guards, RCD/earthing) and post-cut verification, gating every job before, during, and after the cut.

Marble cutter blade lifespan typically runs 80-300 cutting hours on continuous-rim diamond blades, with replacement triggered by segment wear, diamond glazing, or core warping rather than a fixed date. Match blade type to marble hardness, use wet cutting where possible, and inspect segments every 4-

An air pick in steel construction is a pneumatic chisel driven by 90-110 psi shop air for slag removal, weld back-chipping, and rivet work; spec selection hinges on bore size, stroke, blows per minute, and vibration control rather than horsepower. AISC 16th Ed. and NYSDOT SCM govern the downstream p

A formal marble cutter commissioning protocol covers four gates: site readiness, mechanical no-load checks, wet/cold test cuts, and load-cut acceptance against written specs. Documentation of baseline numbers, electrical and water verification, and signed punch lists are non-negotiable before retent

Floor grinders for steel construction typically operate at 1-15 kW with working widths of 230-800 mm and weights from 40 kg to 640 kg, matched to substrate hardness and job size. Planetary and four-disc walk-behind units dominate large-area steel substrate prep, while handheld 4-7 inch models handle

Marble cutters (1450 W class, 220–240 V mains) demand layered controls: ANSI-rated eye and hearing protection, P100/N95-class respirators for crystalline silica dust, RCD protection on damp sites, and a 100 mm-class diamond blade matched to wet or dry cutting.

A total station computes slope distance, horizontal angle, and vertical angle in one instrument, then resolves the target's 3D coordinates via triangulation. EDM runs on laser or infrared time-of-flight, angle encoders resolve to 0.5–10 arc-seconds, and the choice between manual and robotic is decid

An air impact wrench used on HVAC installation should be lubricated with 2 to 15 drops of pneumatic tool oil at the air inlet before each use, with the impact mechanism serviced separately per its own manual, and the compressor fed through a 90 to 120 PSI regulated, moisture-free supply. Deviating f

A marble cutter cuts stone, granite, porcelain and cement with a diamond-tipped circular blade spun by an electric motor, typically at 12,000 RPM or higher, with wet or dry cooling to control heat and dust.

Field-proven shotcrete machine maintenance runs on three pillars: daily wet-mix and dry-mix checklists covering wear pads, swing tubes and water rings, scheduled hydraulic and lubrication service, and a stocked spare-parts bin. Skipping any of the three costs hours of downtime per shift.

A power mixer combines a low-geared high-torque motor with a paddle gearbox to stir viscous building materials at 150-800 rpm from a 1,000-1,800 W input, while in live audio a powered mixer integrates a mixing console and a power amplifier in one chassis to drive passive speakers from a single signa

Circular saw spare parts fall into wear items (blades, brushes, bearings, guards, springs) and dimensional consumables (rip fences, edge guides, depth levers) matched by model and catalog number. Matching by exact part number from the OEM service parts list prevents binding, runout, and guard-retrac

Concrete groove cutters for landscaping span hand-held 133mm wall chasers at 4800W through to 355mm portable slab saws at 4000W and 76.5cc gas cut-off saws. Match power, blade diameter, groove width (15–63mm), and dust extraction to the substrate (paving, cured concrete, reinforced slab).

Circular saw blade life spans 12 to 120 hours of continuous run time, while the machine itself can serve a shop for at least 10 years with scheduled service. Replace the blade on symptom, not on the calendar: burns, slow feed, binding, or glazed diamond matrix are the four hard triggers covered belo

For landscaping pours (patios, walkways, footings, small slabs), a 1.25-3 HP electric internal concrete vibrator on a 1-2.5 in shaft running 11,000-12,000 VPM covers most jobs, while 6.5 HP gas plate tampers handle sub-base compaction. Global market value sits at USD 1.36 B in 2026.

A correct circular saw commissioning routine covers four checkpoints: pre-power mechanical inspection, blade and depth set, 90° shoe-to-blade squaring, and a live test cut. Set the lowest tooth to project no more than about 0.3 cm below the workpiece, verify squareness against a known reference, and

Electroslag pressure welders for demolition shoring and column rebar handling must deliver 200-650 A at 35-45 V across 16-40 mm bar diameters on a 380 V three-phase supply, with a 1,000 A source required above 32 mm to keep weld-collar geometry inside JGJ 18-2012 limits on axial offset and bar misma

Portable circular saw safety hinges on three controllable failure paths: kickback from dull or pinched blades, guard defeat that exposes the spinning arbor, and inadequate PPE for eyes, hearing, and respirable dust. CCOHS, SafeWork SA, and the Power Tool Institute converge on blade depth set 1/8–1/4

Infrared line levels used at HVAC installation fall into two distinct families, audio signal levels (-10 dBV / +4 dBu) and laser leveling tools (635–660 nm class II/IIIa), and the 2026 specification drive ties them to condenser pad flatness, IMC 1109.2.2 line-set protection, and 45–55 dB(A) property

Climbing formwork systems typically deliver 8-15 years of service on high-rise cores when maintenance cycles are honored, with hydraulic self-climbing units reaching 200+ pours per set before major overhaul.

Ride-on power trowels used on concrete slabs around HVAC equipment pads demand a strict daily cleaning and lubrication routine. Field service guidance from BISON, Junqi, and Multiquip fixes the same 5-minute checklist: wash off wet concrete, grease moving parts, change gearbox oil every 50 hours, an

A circular saw cuts by spinning a toothed or abrasive disc around an arbor at high rpm, with each tooth taking a small chip on every revolution. Hand-held, table, miter, and cold-saw variants share the rotary principle but differ in power source, blade diameter, and feed mechanics.

Impact drill bit failures fall into three dominant modes: tip chipping from impact overload and thermal stress, hole drift from rebar deflection, and bit jamming from dust accumulation. Carbide grade, start RPM, and cooling intervals are the primary prevention levers on jobsites.

Impact drill spare parts split into three wear tiers: consumables (chuck bits, driver bits, carbon brushes), service parts (housings, chucks, switches), and major subassemblies (motor, gearbox, hammer mechanism). Match by exact model/serial, not by brand, and keep brushes and chuck jaws as standing

An impact drill pre-use inspection checklist covers chuck seating, bit sharpness, cord/battery integrity, switch trigger, ventilation slots, and excessive vibration, run before every shift. Pass or replace items against documented criteria; do not operate when the chuck binds, the housing shows crac

On-site rebar benders used in landscaping and hardscape builds follow a fixed daily-to-annual maintenance schedule: pre-shift inspection, 2-hour/15-minute duty cycles, ISO VG46 hydraulic oil on a 500 h first change, 2,000 h or annual interval thereafter, and lockout/tagout before any service. Accept

Impact drills typically deliver 3-7 years of service under professional contractor use, with replacement triggered by chuck wear, motor brush or commutator failure, gearbox fatigue, or battery capacity loss below 70-75% of rated spec. Decision hinges on usage intensity: 50-200 hours per year defines

Impact drill safety hinges on a small set of engineering controls: PPE to ANSI Z87.1 and ANSI S12.6, chuck-key discipline, dual-grip control with an auxiliary handle, and verification of concealed services before drilling into walls, floors, or ceilings. Operator-vibration exposure under EN 60745-1

For HVAC duct and sheet-metal installation, OSHA 29 CFR 1910.254 governs arc welder selection, voltage limits (80 V AC manual, 100 V DC), grounding, and supply conductor sizing. Match machine output (amps, duty cycle, OCV) to base-metal thickness and stick/TIG process before evaluating alternatives.

Cut-off machine failures cluster into eight predictable modes: abrasive-wheel breakdown, motor burnout, bearing seizure, spindle runout, guard interlock failure, vibration, coolant starvation, and electrical faults. Roughly 35-40% trace to inadequate lubrication, 18-25% to wear, and 12-18% to instal

Walk-behind concrete power trowels cover 24–46 in. diameters at 5.5–14 hp with adjustable blade pitch, while ride-on units span 1.8–3.7 m (6–12 ft) at 10–70 kW. Selection hinges on slab size, engine class, and pitch-control type.

Cut-off machine spare-parts kits bundle belts, air filters, fuel filters, spark plugs, cords and service tools, while abrasive wheels are graded to 5400 RPM at 14 in diameter. A spec-first parts list keeps downtime predictable.

Concrete vibrator spare parts and consumables cover vibrator heads, flexible shafts, hose assemblies, switches, and lubricants, with Milwaukee MX FUEL heads at $265.72-545.21 and Oztec heads from $184.99. Sourcing per OEM manuals (Multiquip BPX/G55H, Dynapac AN series) prevents downtime on site.

Cut-off machines span fiber laser, CO2 laser, abrasive cut-off saw, pipe cutter, die cutter and digital cutter families, each with distinct service-life bands: fiber laser pump diodes commonly rate near 100,000 hours, CO2 tubes 1,000-10,000 hours, and consumable blades, nozzles and optics are the fi

Pneumatic nail guns cause roughly 37,000 U.S. emergency-room injuries a year, and the injury rate is about 2x higher with multi-shot contact triggers than with single-shot sequential triggers. Cutting that risk is a spec-level problem: choose sequential triggers, cap air pressure at the tool's rated

A cut-off machine is commissioned through staged testing: pre-install inspection, mechanical assembly, electrical and motion diagnostics, no-load verification, and on-load cutting trials against documented parameters. On 2026-08-31 SENFENG released a 30kW fiber laser cutter commissioning case study

Stud welder maintenance in HVAC installation hinges on a daily gun-side discipline and a tiered tear-down schedule: daily chuck and contact-tip inspection, weekly carbon-brush cleaning, and a full gun strip-down every 3 months for heavy users or annually for light users. Cables and power units follo

A cut-off machine separates a workpiece by swinging or feeding a rotating blade through a clamped stock, with abrasive wheels grinding, cold-saw teeth shearing, and diamond wheels grit-cutting. Selection hinges on material, tolerance, heat, and spark class, not brand.

Angle grinder failures split into three families: abrasive wheel break-up (often from exceeding disc RPM rating, missing guards, or wrong wheel for material), tool-side electrical/mechanical faults (carbon brush wear, power-cable damage, switch failure, overload), and operator-side abrasive ruin (gl

Rotary and self-leveling laser levels used in landscaping survive roughly 5-10 seasons of regular outdoor duty when crews follow a fixed maintenance loop: lens cleaning with microfiber, 180-degree calibration checks, dry padded-case storage, battery swap-out before full drain, and IP-rated moisture

Angle grinder spare parts fall into three groups: wear items (carbon brushes, cut-off wheels, flap discs), fasteners (flange nut, inner flange, clamp washer), and safety/control parts (blade guard, paddle trigger, cordset). Spec the parts to the tool's RPM rating and wheel diameter, and replace brus

A sander inspection checklist verifies machine stability, abrasive-belt and disc guarding, dust extraction, and electrical isolation before each shift. Pre-use acceptance items include a 36-inch disconnect clearance, a 1/4-inch disc-table gap, and a functioning mushroom-head emergency stop, per Cali

An angle grinder inspection checklist organises pre-use, in-service and post-use checks across PPE, guarding, electrical, mechanical and disc condition. Key acceptance values: carbon brushes above 5 mm, no disk wobble, no insulation cracks, guard present and adjustable, RCD on supply.

A corded 4.5 in angle grinder averages 5–10 years of service with scheduled carbon-brush swaps every 100–200 hours, while cordless units are battery-bound, typically 3–5 years before the pack dictates replacement.

For HVAC installation, pneumatic nail guns operating between 70 and 120 PSI drive most ductwork fasteners, with framing nailers reaching 400+ PSI for steel-stud work. Pairing a 15- or 16-gauge finish nailer with a 2 CFM at 90 PSI compressor covers residential duct fastening; high-pressure framing na

Angle grinder commissioning follows a fixed pre-use inspection sequence: housing and cord check, brush wear threshold (5 mm), disc rpm vs spindle speed match, guard security, then a no-load test run. Cordless units add a manual disc rotation check before any energised test.

A laser distance meter is commissioned by validating its time-of-flight reading against a known baseline at multiple setpoints, typically confirming ±2–3 mm accuracy over 1–30 m. The standard sequence covers reference-edge setup, power and self-test checks, target acquisition, comparison against an

Angle grinder safety hinges on four checkpoints: certified PPE (Z87.1 eye protection plus face shield), RPM-matched abrasive wheels verified by ring-test, intact wheel guards, and 230 mm (9 in) models are restricted on many sites. Operators must grip both handles and lock out/tag out before disc cha

Landscape-grade concrete placed with a laser screed holds its FF/FL numbers only when the screed head, laser optics, and hydraulics are serviced on a fixed cycle: clean sensors after every pour, torque hardware before and after placement, and recalibrate the laser reference against a known benchmark

Rotary hammer failures cluster around bit slippage, gearbox contamination, slip-clutch wear, and operator vibration injury, all of which are addressable through SDS shank selection, scheduled lubrication, and torque-control features such as Hilti ATC and DeWALT CTC.

Rotary hammer spare parts fall into three groups: wear consumables (carbon brushes, chisel bits, SDS-Plus/SDS-Max shanks), service kits (diaphragm assemblies, O-rings, ball bearings), and structural components (field/armature assemblies, gear housings, pistons). A 1-inch D-handle rotary hammer servi

Stud welders typically deliver 5-10 years of service life on light auto-body duty and 15+ years on construction-manufacturing duty, with replacement driven by capacitor degradation, contactor pitting, and tip wear rather than calendar age. Replace the gun, capacitor bank, or control board when weld

A rotary hammer inspection checklist combines a corded/cordless power-tool safety walk-around with a drill-rig pre-start flow, covering PPE, chuck, bit, brushes, cord and hydraulics on a daily shift basis.

A rotary hammer's working life on concrete is dominated by brush wear, chuck service interval, and impact-energy class: SDS-Plus machines in the 2.0–3.5 J range typically run 500–1,000 hours before carbon-brush service, while SDS-Max 6–12 J units are usually retired at 1,500–2,500 hours or on chuck/

Rotary hammer commissioning is a staged process: visual inspection, electropneumatic function test, SDS chuck and bit verification, no-load run, and load run on a concrete block, with operator sign-off and PPE checks recorded before handover. For Hilti-style EP platforms, the four sign-off

Pneumatic Air Pick consumables break into three families: filter and regulator service kits, lubricant and seal consumables, and mechanical wear parts (hammers, pistons, chisel shanks). Stocking is governed by duty cycle, with 1,000-2,000 hour filter intervals and 500 hour grease points as the worki

Rotary hammer and jackhammer operation requires strict adherence to PPE, vibration management, and dust control protocols. OSHA 1926.300(a) mandates safe tool condition, while 1926.1153(c)(2)(ii) requires wet methods or VDCS to control respirable crystalline silica.

A rotary hammer uses an electro-pneumatic (EP) impact mechanism: a motor-driven drive piston compresses air in a sealed cylinder, launching a flying piston (striker) that strikes an anvil in the SDS chuck, delivering thousands of high-energy blows per minute with far less operator force than a cam-a

Storage rack systems are specified by pallet geometry, beam load rating, upright frame capacity, and a height-to-depth (HTD) ratio governed by ANSI MH16.1. Selective, push-back, drive-in, and pallet-flow racks each suit different SKU counts, FIFO or LIFO needs, and seismic categories. Cold storage a

Workbenches in wood, steel, and stainless variants share a 4-tier maintenance rhythm: daily wipe-down, monthly hardware check, seasonal deep clean, and 6-12 month structural audit. Failure mode frequency and corrective steps are documented across 8 vendor guides published between Feb 2025 and May 20

Work bench installation breaks into three paths: bolt-together steel cabinet systems, build-from-lumber wood frames, and fold-flat portable workmates. Selection hinges on load rating, footprint, fixed-vs-portable duty, and accessory integration with vises and casters.

The oxy-fuel cutting torch market in 2026 is dominated by a handful of legacy brands (Victor, Harris, ESAB, Miller, Tweco, Koike) plus a long tail of regional assembly houses, with cutting capacity, fuel-gas compatibility, and tip interchangeability as the key procurement criteria.

Oxy-fuel cutting tip selection on mild steel runs from size 00 for 1/8 in. stock up through size 4+ for plate to 12 in., with tip bore, preheat orifice, and oxygen pressure all scaling to thickness. Use this 4-step gate (seat type, metal thickness, application, fuel gas) to match torch, tip, and pre

Oxy-fuel cutting torches cut mild steel from 1/8" to 12" thick when sized to the plate; tip seat, preheat flame, gas selection and duty cycle drive the spec. Match the tip to metal thickness, the fuel gas to the application, and the torch body to repeated shop or field use before buying.

Plasma cutter sizing is governed by three spec pairs: rated vs sever cut on the material you actually cut, the 80-20 rule on thickness, and amperage matched to the consumable nozzle. Match duty cycle, primary power, and pierce capability to the workload, not the brochure headline.

For marine-grade cutting, Hypertherm leads the 2026 spec map with Powermax 30 XP through 125 XP systems; mid-range 50–70A inverter units from ARCCAPTAIN, Bestarc, PrimeWeld and Amico cover 1/2" plate at $180–$600. Pick by cut thickness, duty cycle, and input power, not brand alone.

Miller, Lincoln Electric, and ESAB dominate North American TIG welder distribution with 76, 50, and 9 SKUs respectively across major US welding suppliers as of 2026-09-07. Globally, ten manufacturers including Fronius, CIGWELD, Panasonic, and Taizhou Genteck anchor the supply base, with single-phase

Pick a TIG welder by matching AC/DC output, current rating, and duty cycle to the thickest material you will run. For 6 mm aluminium you need 200+ A AC with at least 40% duty cycle; for thin stainless under 3 mm, a 150 A DC inverter suffices.

Pick a TIG welder by first locking the current type (DC only, or AC/DC if aluminum is on the menu), then matching amperage range to your thickest material, duty cycle to your weld length, and input voltage to your shop outlet. A 120V entry unit covers roughly 0.1–3 mm steel; full AC/DC inverter mach

The arc welding machine supply base spans 60+ named manufacturers across the US, Germany, China, Japan, India and Austria, with Lincoln Electric, Miller, ESAB, Fronius, Panasonic and ITW Welding anchoring global demand. Specifiers should match process (SMAW, GTAW, GMAW, SAW, FCAW) and duty cycle to

Arc welder sizing is a four-step gate: pick the process (SMAW, GMAW, GTAW, FCAW), match input voltage and primary current, verify duty cycle at the working output, then size feeders to NEC Article 630. Get any of these wrong and the breaker trips, the cable overheats, or the weld starves for amperag

For landscaping concrete work, select crane-climbed or guided climbing formwork with platform width 2.4–2.8 m, working-load class 3 to 4, and wind rating to 200 km/h. Automatic hydraulic self-climbing only pays off above 100 m or on tall cores.

Climbing formwork for plumbing riser installation is selected against four plumbing-driven criteria: platform load class (Class 3 at 2.0 kN/m² vs Class 4 at 3.0 kN/m²), max single-pour height (1.5-6 m), bracket anchor spacing tied to the wet riser shaft, and gust-wind limit (24.5-28.5 m/s). Cantilev

For interior finishing, the air pick window is a 2-3 kg mid-range chipping hammer at 1500-3000 BPM, 5-10 J per stroke, 12-19 mm hex shank, drawing 12-18 CFM at 90 psi; pick the shank that matches existing chisel inventory.

Power mixer installation hinges on four controlled steps: clear 30 cm ventilation clearance, a fused IEC mains feed on a Class I protective earth, balanced 1/4-inch TRS or XLR audio runs, and a power-to-impedance match between 200-1000 W per channel and 4-8 ohm speaker loads. Skipping any one of the

Cut-off machine total cost of ownership is driven by consumable wheels, motor class (0.8–5.5 kW), duty cycle, and dust extraction, not sticker price. A 1.0 kW precision abrasive unit at $450–$3,300 for industrial plasma variants can swing 3–5× over five years once blades, energy and downtime are cou

For tunnel construction, suspended working platforms are not the primary access system; they are used on tunnel portals, cross-passages, ventilation shafts, and dam galleries where rope suspension geometry applies. ZLP-class cradles rated 250-1000 kg, governed by EN 1808 and GB 19155-2003, fit these

For interior finishing, an air pick sized in the 0.8-1.5 kW, 19 mm or 28 mm hex shank, 900-1500 BPM band with an anti-vibration handle under 5 m/s² is the working window; it is the wrong tool for fine surface prep, where needle scalers and air-assisted airless sprayers take over.

For bridge construction, a 16 in. diamond-blade walk-behind concrete groove cutter in the 50-65 cc 2-stroke engine class is the workhorse pick, delivering 125-130 mm cut depth that matches typical 100-125 mm deck slabs plus overcut. Specify wet-cut with a 30 L on-board tank and a rebar-tolerant diam

Cantilever climbing formwork systems (CB-180 and CB-240 with 180 cm / 240 cm platform widths and 6 m one-pour height) are the spec baseline for tunnel concrete pours, while hydraulic auto-climbing units like QPMX-50 and ZPM-100 fit vertical shafts and chimneys. Select by pour height, lateral pressur

For HVAC installation, select an oxy-fuel cutting torch rated to at least 6 mm to 25 mm mild steel, with a balanced-pressure injector mixer and a Type 41 cutting tip sized to the heaviest plate, fed by 99.5 percent or higher oxygen at 200 to 400 kPa, with AS 4603 flashback arrestors on both oxygen a

ZLP-series suspended working platforms in 500 kg, 630 kg, 800 kg and 1000 kg load ratings are the dominant choice for bridge construction access, with 8.3-10.2 mm wire rope, 9.3 m/min ±5% lift speed, and CE plus ISO 9001 certification. Selection hinges on rated load, platform length, lift height, an

Plasma cutters do not cut concrete, brick, or stone; they cut only the embedded metal on masonry sites (rebar, anchor bolts, mesh) and pair with a concrete groove cutter for the substrate. Pick a 60-100A inverter with 60% duty cycle, 4-6 CFM clean air, and 240V input to cover 3/8-1 in clean cuts on

Pick a walk-behind for slabs under 3,000 sq ft at 3–7 HP, or a ride-on at 24–65+ HP for slabs over 3,000 sq ft. Match blade type (float, combination, finish) to the pass stage, and start the first pass when a footprint is no deeper than 3 mm per ACI 302.1R.

Plumbing laser selection splits into two product groups: rotary grade lasers for setting fall on drainage runs and slab prep, and pipe lasers for laying sewer at 1.667-2% grade. Single grade covers most plumbing; ride-on boom laser screeds suit industrial floors above 1,400 m²/day per pour.

Laser screeds for steel-structure projects are selected by matching head type, reach, drive class, and grade-control method to slab size, FF/FL targets, and site access, with rotating-laser reference the default and 3D total-station guidance reserved for contoured pours. Spec ranges cluster around 1

Walk-behind power trowels in the 36-46 in. (920-1,180 mm) diameter class, 5-14 HP, 60-150 RPM, are the practical default for tunnel invert and sidewall walkways. Diesel, petrol, or LPG engines are chosen against tunnel air-quality rules, not finishing speed alone.

Power trowels for HVAC installation should be picked by floor-area, power source, and rotor diameter: 24-36 inch walk-behind units (5-9 HP, 60-145 RPM) suit equipment-room slabs under 200 m², while 48 inch ride-on trowels (13 HP, 1,220 mm path) fit plant-room pours above 500 m².

For plumbing installation, select walk-behind power trowels in the 600 to 960 mm diameter range with 3 to 5 HP motors, 4 blades, and 50 to 130 RPM blade speed to finish pipe-chase and utility-room slabs efficiently.

For landscaping work, choose a pneumatic-excavation air pick (soil pick) at 80-160 cfm, 100 psi inlet, with a 4 in (10 cm) stand-off for root-zone and trench daylighting, or a pneumatic-percussion pick at 1500-3000+ bpm, 5-35 lb, governed by ISO 11148-4 and OSHA 29 CFR 1910.243. Match nozzle/bore, c

An electroslag pressure welder (EPW) is the wrong tool for HVAC ductwork and pipe support fabrication, where 24-gauge sheet, copper tubing, and aluminum bracketry call for low-heat processes such as TIG and shielded metal arc welding. The EPW domain is vertical rebar 16-40 mm on a 1,000 A class sour

For demolition contractors, the laser screed is the wrong primary tool: it finishes fresh concrete, while demolition is about controlled removal. Pick a boom or ride-on laser screed only if the project is a slab-on-grade replacement with simultaneous pour, sized 1,500+ m², FF 50+ spec, and tracked t

For 2026 masonry crews, a rebar straightener is the wrong primary tool; spec a portable hydraulic rebar cutter (110 V, 10-32 mm class) for footing work, and reserve a coil-fed straightener (1.5-7.5 kW, D6-D16) only for off-site fab yards feeding stirrup or mesh production. Selection hinges on four n

Aluminum ladders are specified by four pillars: duty rating (Class III 100 kg to Class 1 / EN131 Professional 175 kg), working height (0.85 m to 8 m), step geometry (80 mm industrial depth, 304 mm tread pitch on entry-level, 200 mm deep checkerboard on platforms), and the standard they satisfy (EN 1

Air picks (pneumatic chipping hammers) for concrete work are typically specified in the 10-30 kg class, 25-35 bpm strike rate range, and matched to a 0.6-1.2 m³/min air compressor when rebar or heavy aggregate is present. Air-entrained concrete mixes (4-7% entrained air) and silica-dust extraction r

Electroslag pressure welders serve landscaping-scale vertical rebar splicing in retaining walls, garden pillars, and small piers when bars run 16-32 mm, with AC transformer units at 7-16 kg head weight covering most low-volume work. They are not the right tool for thin plate, stainless, or out-of-po

For tunnel construction, specify an electroslag pressure welder with a 16-40 mm bar range, 200-650 A output at 35-45 V arc voltage, and a programmable arc-to-upset timer; below 25 mm plate thickness, the slag bath cannot be reliably established, so EPW belongs on rebar cages, not plate.

For concrete column rebar splicing, select an electroslag pressure welder with a power source rated at 200-650 A arc current, 35-45 V welding voltage, and 70-90 V no-load voltage, sized to your maximum bar diameter up to 32-40 mm. Match the head upset force, current/time schedule per JGJ 18-2012, an

Electroslag pressure welders splice vertical 16-40 mm rebar in cast-in-place piers and abutments under JGJ 18-2012 or AWS D1.4, with selection driven by bar diameter, upset force, and arc-to-upset control sequencing.

For road-maintenance access, pick scaffolding by asset class: walk-through Q235B frames (1219 mm, 42×2.5/48×2.75 mm) for low-rise frontage work, ZLP630-ZLP800 cradles for bridges and noise barriers, and Red-Route-compliant tube-and-coupler sets with permits and pedestrian protection in London.

Wet-process shotcrete machines with adjustable output of 3-9 m3/h and rotor or piston pumping are the standard pick for HVAC duct encasement and rooftop equipment base work; dry-process units suit only small patch repairs under 1 m3/h.

For plumbing installation embedment, wet-mix swing-tube shotcrete rigs in the 3-4 inch class (2-20 yd³/h, 750-2100 psi discharge) are the spec baseline; dry rotary-gun and small peristaltic pumps fit only narrow access or repair work. Match the pump to line size, slump, and embedment geometry before

Tunnel floor grinder selection hinges on three constraints: invert concrete removal depth, ventilation-rated dust suppression, and a power head sized between 5-15 kW for typical 2-4 m road-tunnel passes. Match planetary vs. rotary head, dust class, and power source to whether the work is coating rem

Plumbing-installation theodolite selection hinges on 7" to 10" angular accuracy, 30x erect-image optics, an IP54 rating, and an optical plummet with 0.5 to 1.3 m near-focus for column and anchor-bolt layout on steel and pipework. Erect image and reticle illumination are non-negotiable for verticalit
Air pick selection for steel construction hinges on matching pneumatic chisel output to the bolt, rivet, and concrete-removal duty, with steel air planks rated for point loading above the 60-120 lb aluminum range.
For steel construction, pneumatic nail gun selection hinges on three pressure tiers: standard framing tools (80-110 psi) for light-gauge track, and high-pressure models like the Aerosmith HN120 (rated for heavy-gauge steel and aluminum) and dedicated cold-formed steel tools such as the Model 500 for

For demolition work, an impact drill in the 500–750W class is the wrong tool: it lacks linear concussion for breaking hard materials and is specified for light masonry and screw-driving only. Choose a demolition hammer (medium: 1000W+ for tile and small concrete; large: 1200W+ for slabs) or a rotary

For tunnel construction, marble cutter selection is governed by ground class, UCS, and Cerchar Abrasivity Index rather than the machine name; 17-inch disc cutters suit granite and gneiss at 50-150 MPa, while soft-ground TBMs use 40-60% opening cutterheads with scrapers and bits.

Masonry sanding demands a system, not a single tool: a 150mm planetary grinder with mesh discs stepped P40 to P320, paired to a 130 CFM HEPA extractor, outperforms a random-orbit sander on flatwork, while a 20-grit fluted silicon-carbide rub brick remains the right pick for hand touch-ups on brick a

Cuplock scaffolding is a modular system using a cup-and-blade locking node at 500 mm intervals on the standard, and choosing the right system means matching load class, project geometry, and standards to the four main Cuplock variants. For repetitive facade or formwork bays, Cuplock is typically fas

A suspended working platform's TCO runs 1.8-2.5x its purchase price over a 10-year service life, driven mainly by certification inspections (EN 1808 mandatory every 6 months), wire rope replacement, and operator wages, not the equipment ticket.

For electrical installation work, the 4-inch to 5-inch (115-125 mm) corded angle grinder at 110 V or 230 V, 6-9 A, 8,000-12,000 RPM is the dominant spec. Battery 18 V models suit light tray and trunking only; pneumatic 90-120 PSI units are reserved for hazardous zones.

Rebar straighteners are classified into three drive types, mechanical flywheel, servo-electric, and hydraulic, selected by bar diameter window, line speed, and residual bow tolerance. Standard light coil units cover D6–D16 mm at 30–50 m/min with 1.5–3.0 kW drives, while heavy units reach D32 mm at 8

Rotary hammers use an electro-pneumatic piston mechanism that delivers 2.0-20 J impact energy, drilling in concrete up to 10x faster than hammer drills. They excel at heavy-duty masonry work but cost more, weigh more, and are overkill for light brick or wood tasks.

A 1700 W, 230 V/50 Hz corded demolition hammer ships nearly fully assembled; the only install step on most units is mounting the auxiliary handle and greasing the bit shank, with first relube scheduled at 20 operating hours.

Concrete vibrators split into four primary types: internal (immersion/poker), external (form/shutter), surface (screed/pan), and vibrating tables, with internal units dominating field pours. Head diameters run 25-100 mm, operating speeds span 2,800-15,000 rpm, and correct consolidation can lift dens

US workbench suppliers cluster around four product families: heavy-duty industrial (1,200 lb to 6,600 lb tested), ergonomic height-adjustable, ESD/cleanroom, and wood-shop specialty. Selection hinges on load class, top material, adjustability, and standards compliance (OSHA, ANSI, ISO).

Rebar straightener total cost of ownership in 2026 spans $1,750-$16,500 landed, with motor kW, roller count, energy per ton and consumables as the dominant cost drivers beyond sticker price.

TIG welders for electrical installation should be AC/DC with HF start, 200-300 A peak output, and 40-60% duty cycle. AC capability is mandatory if aluminum busbars or enclosures are in scope, not optional.

For HVAC field crews, an AC/DC TIG welder with at least 200 A output, high-frequency arc start, and a 40% or higher duty cycle is the minimum practical spec, because most HVAC jobs mix thin-wall stainless with aluminum coil/header work. DC-only units are limited to steel and stainless, while AC is m

Bridge construction demands AC/DC TIG machines with 200–400 A output, 3-phase 380–480 V input, and HF arc start; inverter-based full-bridge designs with pulse control dominate site welds on stainless rebar, aluminum deck panels, and structural chrome-moly tubing.

Oxy-fuel cutting torch selection in tunnel construction is driven by OSHA 1910.253's 15 psig / 30 psia acetylene cap, four tip-selection factors (seat type, metal thickness, application, fuel gas), and acetylene vs propane tradeoffs, with strict ventilation and flashback controls governing confined-

For landscape crews, a 120V inverter stick welder rated 20-140A handles gate repairs, trellis fabrication, and thin-gauge steel. Choose a dual-process stick + flux-cored unit for outdoor versatility.

For tunnel construction, diesel-engine MMA/SAW welders dominate because they tolerate damp, confined, poorly ventilated spaces. Inverter-based models with PFC and 60% duty cycle at 200–500 A handle rebar, gantry steel, and water-stop splicing.

Spec a TIG welder for concrete work by matching AC/DC output, amperage range, and duty cycle to the embedded metal being welded: rebar ties in mild steel need a 200 A DC machine, while aluminum embed plates and formwork hardware require AC/DC at 200-250 A with high-frequency arc start. Skip small 11

TIG is the precision process, not a demolition workhorse: for cutting, separating, and rough dismantling jobs, plasma or oxy-fuel lead on speed and cost. Pick a TIG only when the demolition phase also includes thin-gauge stainless, aluminum, or chrome-moly rework where arc control under 10 A matters

Aluminum is the most common portable ladder material per Cal/OSHA guidance, but a 10 ft aluminum ladder weighs roughly 30 lb versus heavier fiberglass. For masonry work, pick the duty rating and configuration first, then verify the unit meets ANSI A14.2-2007.

Type IA (300 lb) or IAA (375 lb) aluminum ladders in 8-28 ft reach are the dominant HVAC install picks, with crossover platforms and multi-position hinges solving rooftop RTU access. Skip aluminum within 10 ft of energized lines: fiberglass non-conductive builds are the only defensible choice in tha

For steel construction, the right arc welding machine is a stick (SMAW) or flux-cored (FCAW) unit in the 200-300A class with 60% duty cycle, because site welds on structural plate, rebar, and beam splices demand deep penetration, wind tolerance, and portability above cosmetic bead quality.

Interior finishing crews welding thin-gauge studs, conduit hangers, and miscellaneous embed plates should default to a 120V MIG machine (20–220A output) for mild steel up to ~3 mm, keep a 120V TIG (20–160A) on standby for stainless/aluminum trim, and treat stick welders as a last resort because flux

Stick (SMAW) and flux-cored arc welders dominate masonry repair and on-site fabrication because flux-shielded rods tolerate wind, mortar scale, and surface rust that defeat gas-shielded processes. Match electrode class (E6011, E7018) and 200–400 A output to rod diameter and steel thickness, with 230

Aluminum extension ladders rated Type IA (300 lb) or higher are the dominant pick for road-maintenance crews needing 16-40 ft reach: roughly 30 lb for a 10 ft unit, corrosion-resistant, non-sparking, and OSHA/ANSI compliant. Skip aluminum near energized overhead lines; specify fiberglass there. Insp

Aluminum ladders in the 6-12 ft stepladder and 16-40 ft extension ranges dominate concrete work, with 10 ft aluminum models weighing roughly 30 lb vs comparable fiberglass near 50 lb. Spec an ANSI A14.2 (metal) / Cal/OSHA T8 CCR 3276 ladder at Type IA 300 lb duty rating or higher for rebar tying, fo

Suspended work platforms (SWP) for HVAC installation are selected on five hard criteria: rated load + crew count, working height vs. suspension height, footprint geometry, fall-protection class, and project mobility. Two-point adjustable (swing stage) units dominate when crews move along a façade; m

For steel-frame high-rise cores, hydraulic self-climbing formwork (SCE) is specified above ~15 storeys; crane-dependent systems suit low-rise cores under 8 storeys, while single-sided climbing is reserved for dam/pier walls. Selection pivots on cycle time, wind exposure, anchor pull-out capacity, an

Climbing formwork selection for interior finishing hinges on shaft geometry, wall thickness, lift height, and crane access: interior climbing systems with recoverable box anchors suit hollow columns and stair/elevator cores; hydraulic self-climbing rigs win on tall cores. Typical lifts run 3–4.5 m p

Climbing formwork for demolition work calls for crane-independent self-climbing or rail-guided systems with hydraulic rams, since demolition sites restrict crane reach, demand wind-tolerant lifts, and need stable anchoring to existing concrete. Crane-climbed jump forms stay viable for low-rise, low-

Climbing formwork selection for masonry is driven by structure height, geometry variability, and crane availability. Self-climbing (hydraulic) systems suit cores and tall piers, crane-lifted systems suit mid-rise walls, single-sided systems suit dams, and section-by-section suits geometry-changing s

Select a suspended working platform for electrical installation by matching rated working load, working height, and platform length to cable tray, conduit, and lighting work; electric hoist units (1.5–3 kW class) suit most low-rise jobs, while 5 kW+ twin-hoist gondolas handle high-rise façade cable

Cantilever climbing formwork is not the right tool for typical road maintenance: select jump-form or single-sided climbing systems only for bridge piers, abutment walls, and retaining structures above 6 m, where vertical repetition and high concrete pressures rule out conventional gang forms.

For concrete walls above 15 m, choose self-climbing (hydraulic) formwork when crane access is restricted, height exceeds 30 m, or cycle time must drop below 4 days per lift. Pick crane-climbing formwork for repetitive low- to mid-rise cores, single-sided variants for dam and retaining-wall pours.

Line laser levels (also called line generators) are the correct tool class for interior finishing, projecting a 180° to 360° reference plane for chair rails, drop ceilings, cabinetry, and trim within the typical indoor working range of 1–150 feet.

For steel-construction layout, an infrared line laser covers interior fit-out at 30-100 ft; outdoor steel erection and grading at 200+ ft still needs a rotary laser with a detector, not a line generator.

Steel scaffolding is selected for steel construction by matching steel grade (Q235/Q355 or S235/S275/S355) to load, height, and site exposure, then pairing it with OSHA-compliant fall protection above 3.1 m. Steel outweighs aluminum roughly 3:1, so it is preferred for heavy structural work, while al

For HVAC installation at height, mobile tower or Kwik-Stage modular scaffolding (SANS 10085 / OHSACT compliant) suits ductwork and unit placement, while DTU 43.1 galvanized terrace frames (41×41×2.5 mm, 500–1500 kg load) handle rooftop equipment. Match scaffold duty rating to load class and roof typ

Infrared line levels for electrical installation pair visible laser line generators (typically +/- 60° to >180° fan angle, self-leveling within ~4°) with thermal-imaging verification of energized gear. The optimum tool is a self-leveling line laser for layout plus a thermal imager sized to the small

For plumbing installation, an infrared line laser is the right tool when the job is indoor, short-range, and layout-driven: pick a self-leveling cross-line unit (with plumb points if verticals matter) for rough-in, sink brackets, and ceiling transfers; step up to a rotary laser only for outdoor sewe

For masonry layout, line-generators cover 1–150 ft runs and rotary lasers with a detector extend to roughly 700 ft, with self-leveling ±0.0002 in/in accuracy and green beams visible 4x over red at the cost of ~2.5x shorter battery life.

For landscaping, choose a theodolite (or auto level) with 20x-32x magnification, a 360-degree horizontal scale, and stadia reticle for cut/fill work, matching instrument to slope distance and tolerance rather than buying on price alone.

Steel-construction elevation control most often specifies an optical automatic level with 24x to 32x magnification, a compensator working within ±15 arcminutes, and 1.5 mm/km double-run accuracy, since the auto-compensator self-relevels and reduces setup time by roughly 30% versus manual instruments

For demolition work, automatic levels with 24x to 32x magnification and ±1.5 mm accuracy at 45-76 m are the standard spec band, paired with magnetic-dampened compensators on IP54-rated bodies. Laser variants with self-leveling compensators now dominate because they tolerate ground vibration, tempera

For interior finishing, specify a laser distance meter with 20-40 m range, ±1/16 in (±1.5 mm) accuracy, green-beam visibility, Pythagorean and area modes, IP54+ ingress, and Bluetooth export. Match class to task: pocket 30 m for trim, mid-range 50 m for rooms, long-range 100 m+ for as-built.

For interior finishing, pick an automatic level by matching the project's finish tier (Q1-Q5 drywall) to instrument accuracy: rotary laser levels suit large rooms and suspended ceilings, while optical automatic levels with 1.5-2.5 mm/km accuracy handle fine trim and cabinetry layout.

For a 35 mm wide, 25 mm deep channel in masonry, a dual-blade wall chaser at 1100–4800 W with adjustable depth and dust extraction is the practical choice; expect repeat cuts under 5 m to run cleanly, with hire-grade twin-blade units delivering the straightest finish.

Total stations selected for interior finishing should deliver 1-3 mm accuracy, a 350-500 m prism range, and motorized tracking when one-person layout is needed. For sub-millimeter partition and ceiling work, manual or 1 arc-second robotic total stations outperform laser scanners and GNSS on enclosed

Concrete groove cutter selection comes down to four decisions: floor versus wall, power source (electric vs walk-behind ICE), blade diameter (5 to 14 in), and dust control. Hand groovers fit joints under 1/2 in deep; wall chasers run 4800 W for vertical slots; ride-on groovers serve large industrial

For demolition work, pick a concrete groove cutter by carrier class: 2-6 t mini-EX with a wall chaser or KDS diamond saw for indoor chase work, 15-30 t mid-size EX paired with DMW cutter wheels for cut-and-break productivity at 4-7x rock-breaker output, and 30-60 t EX/DMW for slabs and bunkers above

Wet-mix robotic shotcrete machines (5-21 m³/h) outperform dry-mix rotor/stator units for electrical-installation embedment, where 208/230V electric drives (5.5-15 kW), 360 psi pump pressure, and 1.5-2 inch delivery lines dominate the decision map.

For 2026 concrete work, spec a self-leveling rotary laser with at least ±1/8 inch accuracy at 100 ft, a 600–2,600 ft working range, and IP66 rating. Green beam is preferred indoors, red beam with detector outdoors, and dual-slope models handle grade work beyond flat slabs.

Electroslag pressure welding (EPW) does not fit plumbing-pipe installation. The process is engineered for vertical column rebar 16-40 mm under JGJ 18-2012 and AWS D1.4, not thin-wall tube 0.065-0.25 in (1.65-6.35 mm). Specify TIG (GTAW) or MMA (SMAW) 130-250 A for plumbing tie-ins; reserve EPW for c

Electroslag pressure welders splice vertical rebar in demolition shoring columns at 16-40 mm bar diameters, with 600 A at 40-50 V and 1,000 A for bars above 32 mm. Plate ESW is a different process and rarely fits demolition work.

For demolition and structural-alteration work, rebar couplers are selected on ISO 15835 compliance, bar-end prep method, and rotation access, with Type A/B/C installation maps driving field choice. Threaded and shear-bolt systems dominate; grouted sleeves suit precast and confined spaces. Capacity t

Electroslag pressure welding (ESW) welds carbon and low-alloy steel from 19 mm upward in a single vertical pass, with low H₂ risk but coarse-grain HAZ. Best fit: thick box-column diaphragms; wrong fit: thin plate, impact-critical zones, or any need to stop mid-joint.

For road-maintenance crews splicing vertical column rebar on bridge piers and abutment stems, the right electroslag pressure welder in 2026 is an inverter DC unit with 16-40 mm bar range, 200-650 A current, and a programmable arc-to-upset timer, governed by JGJ 18-2012 in China and AWS D1.4/D1.4M in

Tunnel rebar splicing is shifting from lap splices to mechanical couplers, with threaded and cold-extrusion systems dominating on shafts, crown bars, and segmental linings. Selection criteria are bar size, fatigue/seismic class, water ingress, and code compliance under ISO 15835 and ACI 318.

Electroslag pressure welder selection for interior finishing centres on bar diameter 16-40 mm, no-load voltage 70-90 V, current above 1,000 A for 32 mm+ bars, and a flux-filled upset head, all governed by JGJ 18-2012 and AWS D1.4/D1.4M.

For electrical-installation column rebar, electroslag pressure welder (EPW) selection hinges on bar diameter range, no-load voltage of 70-90 V, and 1,000 A capability above 32 mm per JGJ 18-2012. Match the head to a current/time schedule and the right flux rather than buying the largest kVA cabinet

Landscaping rebar jobs typically need a 14-32mm rebar threading machine, where a 5.5kW thread-rolling unit out-performs a chaser cutter on joint strength, surface finish, and on-site productivity.

For landscaping rebar work, pick a rebar straightener sized to the bar diameter on the cutting list (typically D6-D16 mm coil, 1.5-7.5 kW motor) and the daily cuts per shift, not by brand. Electric bench/cutter-straightener combos at 48.0% power-source share cover most edge-restraint, tree-anchor, a

Rebar threading machines for masonry splice work typically cover 16mm to 40mm bar diameters, with roll-rolling units hitting 20-30% tensile gain and 50-200% corrosion gain over cut threads. For masonry crews, a 4.0 kW portable rolling head with integrated rib-stripping is the most common match.

For bridge construction in 2026, select a rebar threading machine rated 3-7.5 HP, 1440 RPM, 415 V three-phase, sized to your rebar diameter (typically 16-40 mm), with rib-stripping plus thread-rolling in one pass. Specify automatic models for high-volume pier or deck work, chaser machines for large-

Rebar threading machines for demolition cuts sized 16mm to 40mm bars, with heavy chaser units covering 8mm to 65mm. Pick by bar diameter, threading length, motor class, and site power: 415V three-phase for stationary rigs, portable units for mobile demo crews.

Rebar straightener selection for electrical-installation work depends on bar grade, diameter range, and throughput: a 1.5–7.5 kW mandrel-drive straightener with 4–6 rollers is the right pick for HRB400E 6–16 mm coil feed, and 30–50 m/min line speed, holding ≤2 mm/m straightness for threading into co

For road-maintenance splicing in 2026, select a rebar coupler by matching bar grade and diameter first, then load class, then site access. Standard threaded or shear-bolt couplers dominate routine pavement and bridge-deck repairs, while grout-filled and swaged types handle precast starter-bar and co

HVAC-installation rebar straightener selection runs in two narrow bands: 1.5-3.0 kW portable units for #3-#5 bar in 90-180 kg single-phase frames, and 5.5-15 kW stationary YG-class machines on 380 V three-phase for coil feed at 30-55 m/min. Match motor kW to bar diameter, voltage to site supply, and

For demolition rebar straightening, handheld battery tools (e.g. RD8-20, max #6/20mm, 18.5 lb) suit confined spaces, while bench rotor machines (Ø6-25mm, 7.5-15 kW, 20-35 m/min) handle scrap-yard volume. Match the tool class to bar diameter, throughput, and mobility.

Interior finishing crews that need to correct bent or coiled rebar on site should match a straightener's diameter range, straightening-hole count, and power source to the bar stock actually being handled. Bench-model ET-series roller straighteners cover 6-25 mm rebar at 4-15 kW; portable hydro-elect

Rebar straightener selection for road maintenance hinges on three coupled gates: bar grade (A615 grade 40 to 80), coil diameter range (commonly D6–D16 mm), and daily tonnage. For road crews running under 30 t/month on light coil, handheld or 1.5–3.0 kW bench units fit; heavy 5.5–7.5 kW dual-motor fr

For rebar bender selection on concrete work, match the tool class to bar size, bend count, and code radius: manual hickey or bench units for #5 (16 mm) and below; electric or hydraulic benders for #6 (3/4 in) to #8 (1 in) Grade 60 work; CNC automatic benders for high-volume stirrup production. ACI 3

Air pick selection for tunnel work hinges on three decisions: pneumatic versus hydraulic drive, pick energy class (typically 30-60 J per stroke), and air supply matched to the tool's consumption at the working pressure (usually 0.5-0.7 MPa). Match these to face geometry, ventilation limits, and grou

For HVAC installation, select a rebar bender rated 1 inch (25 mm) or larger, 110-240 V single-phase, 900-1500 W, cycle 2.5-5 s per 90 deg bend, and CSA/CE listed. Hydraulic electric 6-32 mm models fit most rooftop pad and equipment anchor work.

Pneumatic air picks are matched to bridge construction by material, chipping volume, and vibration/ATEX class; gantry cranes lift 50-900 t precast segments, while air picks handle 1-15 kg class chipping of concrete, rebar descaling, and timber-bridge hardware removal. Wrong picks stall production; r

Air picks for masonry work run on 90 psi shop air at 1,500-2,000 bpm with a 2.5 kg handheld weight class, and the right tool depends on shank style, brick type, and joint hardness.

For landscaping builds, pneumatic nail guns with 15-16 gauge framing or 18 gauge brad/finish capability cover 90% of fastener decisions. Match gauge to substrate: 2-3.5 inch nails for sleepers and frames, 1-2 inch for trim, and always pair with a properly sized air compressor and hose.

For plumbing installation, a 3/8" drive air impact wrench (60-250 Nm) fits most under-sink and fixture work, while a 1/2" drive (200-1,200 Nm) covers main-line and backflow preventer assemblies. Size the tool by the largest fastener on the job, not by average, and pair it with a 6.2-8.3 bar compress

For plumbing installation, a 15 to 16 gauge angled pneumatic finish nailer at 70 to 120 PSI driving 1-1/2 to 2-1/2 inch nails is the most spec-correct choice for trim, blocking and bracket work. Framing and roofing nailers are wrong tools for this trade, while brad and pin nailers lack the holding p

For electrical-installation stud welding, capacitor-discharge (CD) units are the default pick for thin stainless or mild-steel enclosure panels, while drawn-arc machines cover larger-diameter cabinet and bus-bar studs. Match stud material to the substrate, plan for one-sided access, and confirm shie

Stud welder selection for tunnel construction hinges on drawn-arc systems for headed concrete anchors and shear connectors, with stud diameters 1/2–7/8 in dominating segment installations. Tunnel environments demand compact, portable guns rated for confined-space work, with daily operator qualificat

For landscaping work, a portable capacitor-discharge (CD) stud welder rated 1-10 mm stud diameter is the standard pick: light enough for one operator on uneven ground, gentle on thin galvanized or painted steel used in planters, edging, and trellis frames. Drawn-arc units are reserved for jobs where

Capacitor Discharge (CD) stud welders are the default pick for HVAC duct and panel work, with M3–M8 stud range and 1–3 ms weld times suiting thin galvanised sheet, while Drawn Arc (DA) units handle heavier M6–M25+ structural fastening. Match process to base metal thickness, stud diameter, and joint

For plumbing installation, capacitor discharge (CD) stud welders in the M3 to M8 (3-8 mm) range suit thin-wall pipe hangers and bracket clips, while drawn-arc stud welders handle M10+ anchors on structural steel. Match process to base-metal thickness, duty cycle, and code path under AWS D1.1.

Sander selection for tunnel construction is governed primarily by rock mass behaviour, water inflow, and excavation method: dry/wet wall sanders dominate in NATM and drill-and-blast headings, while hand-held rotary and belt sanders are restricted to surface finishing on steel arches and precast segm

Stud welding attaches fasteners to masonry-anchored steel plates and concrete embed plates using drawn-arc (DAW) or capacitor-discharge (CD) processes per ISO 14555 and AWS D1.1 Clause 7. Selection hinges on stud diameter, base-metal thickness, current band, and the masonry fastening class (light, m

For interior finishing, capacitor-discharge (CD) stud welders dominate thin-gauge trim, HVAC, and panel attachment, while drawn-arc systems serve structural framing. Selection pivots on stud diameter (M3–M10 typical for trim), base-metal thickness (0.5–3.0 mm), and alloy compatibility. Use CD below

For concrete work, the correct stud welder choice is a drawn-arc (arc) stud welding machine rated for thru-deck shear connector welding, not a capacitor discharge (CD) unit. Drawn-arc handles 12-25 mm headed shear studs through metal deck into beams; CD tops out near 10 mm and is restricted to thin

Drawn arc stud welders covering M6 to M25+ diameters are the standard pick for steel construction, while capacitor discharge (CD) units handle M3 to M8 thin-sheet work. Match process, base-metal thickness, and stud alloy before specifying a power source, gun, and earth-clamp set.

Stud welding on road maintenance projects requires automatically timed stud welding equipment per Iowa DOT IM 558, with stud diameter, base material thickness, and current/time ranges driving welder selection. Capacitor-discharge (CD) and drawn-arc stud welders cover the typical 10–25 mm stud range,

For bridge construction, sander selection is driven by substrate and span: random-orbit sanders (125-150 mm pad, 750-1,200 W) cover deck plate prep, while long-board (矩形砂光机) 矩形 长板 (rectangular long-board) sanders handle 1.8-2.3 m pier-cap fairing. Match abrasive grit (P40-P120) to steel versus concr

For plumbing-installation sander selection, the working envelope usually fits a 5 inch random-orbit cordless platform with variable 7,000-12,000 OPM, a 1/8 to 3/16 inch orbit, and dust-port compatibility for PVC and copper finishing; selection turns on stroke length, vibration, and vacuum integratio

Power mixer selection for HVAC installation hinges on matching motor power and thrust to airflow volume, duct geometry, and fluid resistance, not on raw horsepower. Three-phase AC drives above 3 HP, CFD-optimized static air mixers in galvanized or stainless steel, and explosion-proof enclosures for

For plumbing installation, a demolition hammer in the 1,500-2,200 W, 1,300-1,900 bpm range with 30-50 J impact energy covers most slab and wall-breaking tasks; sub-1,000 W models fit only light chase work, and full 75-90 lb jackhammers are overspec for indoor service-line runs.

For HVAC installation, the right demolition hammer is a 1,300-1,500 W corded SDS-Max or hex 28 J-class unit in the 10-15 kg weight class, because duct and condensate-pipe openings in concrete and masonry need impact energy of 8-16 J, not rotary-drill speed. Match power source (electric vs pneumatic)

Industrial power mixers for electrical installation are sized by ATEX/IECEx zone, IP rating, supply voltage, and locked-rotor inrush, not by motor nameplate alone. A 75 kW mixer drawing 130 A at 400 V can spike to 6–7× inrush, forcing transformer and cable upgrades. Match Ex rating, IP class, and VF

Steel construction sander selection resolves into four families matched to substrate and task: random-orbit 125-150 mm pad for weld blending, 75 mm inline belt for seam grinding, 75-100 mm angle grinder flap discs for heavy stock removal on 6-25 mm plate, and detail/filament for tight corners. Match

Power mixer selection for bridge construction hinges on matching drum capacity, motor power, and mixing technology to grout, mortar, and UHPC batch volumes. Portable drum units cover 3-8 cu. ft. jobs, while planetary and twin-shaft mixers serve high-performance structural concrete. Plan around power

Tunnel work splits hammer selection into two regimes: hydraulic attachment breakers for face advance and mass rock, and compact robotic or handheld breakers for lining removal and confined-section demolition. Choose by mass class, blow energy, power source, and operator-safety distance.

For 2026 bridge construction demolition, electric demolition hammers in the 10-16 kg class with SDS-Max chucks and 1500-2000 W input are the practical spec for deck and pier-concrete breakout, while pneumatic and hydraulic breakers remain the workhorses for continuous pavement and heavy substructure

SDS-Max demolition hammers in the 10-15 kg class are the dominant choice for steel-construction site prep, with TE-Y/HEX-28 chucks, Active Vibration Reduction, and 1000-3000 W impact energy defining the 2026 spec window. Cordless 22V Nuron units now reach 65.7 lb (30 kg class) for floor work.

For electrical installation work, a 7-1/4-inch corded 15-amp in-line circular saw covers most cable-tray, conduit-strut, and panel-board cuts, while an 18-20V cordless rear-handle worm-drive is the go-to for live-site conduit and unistrut work where no outlet is available.

For interior finishing, pick a demolition hammer in the 5-10 J impact energy class, weighing 5-7 kg, with a flat or wide chisel, and confirm low-vibration ergonomics before purchase.

For masonry demolition, SDS-max demolition hammers in the 15–75 ft-lb impact-energy class and 1500 W+ input-power range are the dominant specification; pair tool class with chisel type and vibration control, not just brand.

For plumbing installations, a 110mm wet marble cutter with 1200–1500W input and 30mm cut depth handles ceramic, porcelain and stone pipe-sleeve rebates cleanly. Match motor class to duty cycle, never use dry-cutters on stone, and verify water-feed + double-insulation before site work.

For HVAC installation, a 1400–1600 W corded marble cutter with a 180 mm diamond blade, 5000 RPM no-load speed, 60 mm cut depth, double insulation, and wet-cutting support is the practical field-spec baseline; CNC waterjet is reserved for shop prefabrication of stone housings, not on-site duct or ple

Diamond-bladed wall and wire saws dominate tunnel excavation, while handheld circular saws handle invert trimming, utility cuts, and formwork. For tunnel crews, blade bond hardness matched to aggregate, water-managed wet cutting, and rail-guided wall saws are the three non-negotiable spec axes.

For landscaping cuts, a 7-1/4 in. sidewinder circular saw with a 15-amp corded motor or an 18-36V brushless cordless model covers 2x dimensional lumber, composite decking, and root timber. Match blade tooth count to material: 24T for fast rip cuts in pressure-treated lumber, 40T+ for clean trim cuts

For bridge construction, a corded 18V-class impact drill with at least 60 Nm hard-joint torque, a 13 mm keyless metal chuck, and an SDS-Plus option covers most on-site reaming and anchor-bolt work. Above 20 mm into rebar-bearing concrete, spec a rotary hammer instead. Verify chuck, clutch and duty-c

Standard 7-1/4 inch wood-rated circular saws can cut masonry only when fitted with a diamond or abrasive masonry blade; the choice among segmented, continuous-rim, turbo and abrasive rims is governed by material hardness, wet/dry duty and arbor match.

For interior finishing in 2026, an impact driver (not an impact/hammer drill) is the right primary tool, with a brushless 18V cordless drill kept as backup for hole saws and larger diameters above 25 mm.

For steel construction, use a 0-2500 RPM screw gun with adjustable clutch and minimum 6 amp draw; impact drivers over-torque self-drilling screws above the 2000 RPM screw limit and 900 RPM stainless cap, per MCA and CSSBI guidance.

For landscaping cuts on stone, brick, pavers and rebar, a 4.5–5 inch (115–125 mm) corded angle grinder in the 700–1100 W range, paired with a diamond masonry blade, is the spec-first default. Go to a 7–9 inch (180–230 mm) brushless corded unit for paving slabs and rebar, and pick a brushless 18V+ co

Cut-off machine selection for plumbing installation hinges on matching the cut-off machine, blade type, and motor class to the pipe material, diameter, and job volume. Abrasive wheel, cold saw, and band saw platforms each cover a different duty band, and the wrong combination burns blades or workpie

For steel construction, a 7-inch corded angle grinder with 2000–2600 W input and a no-load speed near 6600 RPM is the default spec; step up to a 9-inch (2-3/4 in cut depth) for heavy section work, and down to a 4.5–5-inch brushless cordless for fit-up, weld prep, and overhead tasks.

For plumbing installation, the SDS-Plus cordless rotary hammer in the 18-26V class, 1.5-2.5 Joule impact range, is the correct primary choice for anchor holes, pipe hangers, and block-wall penetrations. Match chuck size to bit diameter: SDS-Plus for holes up to 26 mm, SDS-Max for larger demolition.

Rotary hammers for tunnel work are typically 1500 W SDS-max class units driving 12-45 mm bits, selected by geology class and shank, not raw impact energy. For drill-and-blast or bolt-hole cycles in confined headings, top-hammer and DTH rock drills generally outperform handheld rotary hammers, which

Mobile scaffold towers come in four core configurations (foldable, single-width, double-width, heavy-duty) and two materials (aluminium, GRP), with EN 1004-1 capping free-standing height at 12 m indoors and 8 m outdoors. Selecting the right unit is a load-class and site-geometry decision, not a bran

Frame scaffolding selection comes down to four decisions: match frame style to existing fleet (Safeway, Waco, or Bil-Jax pin geometry), pick a frame shape (Walk-Thru vs. Ladder) for the access pattern, verify load tier (25/50/75 psf) and OSHA 4:1 height-to-base ratio, then weigh frame against system

Cuplock scaffolding is a modular system with a cup-and-wedge node that joins up to four ledgers per standard at fixed 500 mm centres, favoured for fast repetitive erection on straight façades and heavy formwork. Against general scaffolding (tube-and-coupler, frame, Kwikstage, Ringlock), it trades mu

Match a mobile scaffold tower to the job by sizing platform height to reach (target 1.5-2.0 m overhead), picking aluminium for portability, GRP near live electricity, steel for heavy load, and verifying BS EN 1004 compliance plus PASMA-trained erectors.

A mobile scaffold tower is a wheel-mounted, prefabricated access platform intended for short-duration, frequently relocated tasks up to roughly 12 m, while traditional scaffolding is a tube-and-coupler or system scaffold built around a structure for long-duration work. Selection hinges on duration,

TIG and arc (stick) welding both use an electric arc to fuse metal, but they diverge on electrode type, precision, and operator cost. Pick TIG for thin, non-ferrous, cosmetic-critical work; pick arc for thick, dirty, outdoor structural steel. Tungsten's 6,000°F melting point drives the difference [S

Global laser welding machine suppliers cluster around three hubs: Germany (Trumpf), the USA (Coherent, IPG Photonics, LaserStar, AMADA WELD TECH, Laser Photonics), and China (Herolaser, SENFENG, Han's Laser). Selection hinges on laser source (fiber vs Nd:YAG vs diode), power class, automation depth,

DirectIndustry lists 25 manufacturers offering 46 spot welding welder models, with output currents spanning 25 A to 24,000 A and frequencies from 0.1 kHz to 500 kHz across the catalog. North American supply is anchored by Taylor-Winfield, T. J. Snow, Spot Weld Inc., and Pro Spot, while TECNA, Miller

US-built industrial hose reels from Hannay, Reelcraft, Coxreels, and Duro dominate the North American spec channel, with spring, hand-crank, and motor rewind options. Selection hinges on hose ID, working pressure, retraction duty cycle, and media compatibility, not brand alone.

Rotary hammers and demolition hammers serve different jobs: rotary hammers combine rotation with 1.5–20 ft-lbs impact for drilling, demolition hammers deliver pure 15–75 ft-lbs impact for breaking concrete. Pick by duty cycle, impact energy, and bit-chuck compatibility.

DTH (Down-the-Hole) rigs place the pneumatic hammer directly above the bit for hard, deep rock drilling over 20 m, while top hammer rigs strike from the surface through the drill string for shallower 25–127 mm holes. For abrasive granite, basalt, and limestone above 200 MPa UCS, DTH preserves nearly

Magnetic base drills and impact drills solve different problems: a mag drill anchors to ferrous steel with an electromagnetic base to drive annular cutters on installed structural work, while a cordless impact driver pairs a 1/4-inch hex collet with a hammer-and-anvil mechanism for high-torque faste

Hydrostatic level transmitters use a submerged pressure cell to infer level from the liquid column, ideal for clean liquids and slurries in vented tanks. Laser level transmitters use time-of-flight on a narrow light beam aimed at the surface, ideal for bulk solids, opaque liquids, and aggressive env

Cuplock scaffolding is a modular steel system using cup-and-blade locking nodes on 48.3 mm verticals, with European origin (SGB) and major manufacturing hubs in China, Europe, and the USA. Verified 2025 supplier lists identify SGB, PERI, MJ-Gerüst, RMD Kwikform, and ULMA as the leading European make

TIG welding machine total cost of ownership spans $500 to $15,000 in capital, plus shielding gas, tungsten, electricity, and consumables that typically add 8-15% of purchase price per year across a 7-10 year service life.

Ringlock scaffolding is a modular system built around welded rosette connectors spaced at 500 mm on the vertical standard, accepting up to 8 ledgers/diagonals per node and locking them with hammer-driven wedges. It is the preferred system scaffold for high-rise, industrial, offshore, and event-struc

Plasma cutting uses an ionized gas jet above 20,000°C to slice any electrically conductive metal up to 50 mm cleanly, with maximum severing capacity around 150 mm. Compared to oxy-fuel, plasma runs up to 12x faster on thin stock and 2x faster up to 25 mm, with a smaller kerf and lower HAZ, at the co

Infrared line levels install in five sequenced steps: lock the pendulum, mount on a flat surface or tripod, switch on, allow 1-2 minutes for self-leveling, then transfer the line to the work surface with tape or pencil marks before locking off again. Acceptable accuracy on a 50 ft run sits between ±

Concrete groove cutter purchase price typically accounts for only 20-30% of total cost of ownership, with blade consumables, fuel, silica-control compliance, and downtime driving the remaining 70-80% across a 5-10 year service life.

An automatic level is an optical surveying instrument that uses an internal compensator to keep the line of sight horizontal after a rough bubble-leveling, with telescope magnification of 20× to 32× for survey-grade models. The four common classes are dumpy, tilting, self-leveling (automatic), and d
An automatic level is a self-compensating optical instrument for establishing and verifying horizontal planes on construction sites. Field installation centers on tripod stability, circular-bubble coarse leveling, two-person rod reading, and a 4-step routine that keeps internal compensators in range

Automatic (auto) levels use an internal compensator to self-level the line of sight, giving surveyors faster, more reliable readings than dumpy levels. Trade-offs: no vertical-angle measurement and weaker horizontal-angle accuracy than a theodolite.

A shotcrete machine's purchase price covers only 20–30% of its total cost of ownership, with the remaining 70–80% driven by wear-parts, fuel, maintenance, and downtime. Lifecycle cost per cubic meter sprayed is the correct decision metric, not sticker price.

Suspended working platforms split into single-point, two-point (swing stage), multi-point, modular, and powered variants, each matched to load class 150-1500 kg, anchorage geometry, and facade or shaft work. Selection hinges on rigging-point count, load limit, and drive type.

Mechanical rebar couplers deliver direct bar-to-bar load transfer at roughly 125% the capacity of lap splices, cut rebar congestion in column-beam joints, and reduce total steel, freight, and crane time on congested or seismic projects, at the cost of skilled labor, special bar-end prep, and strict

Rebar threading machines split into three working classes: chaser/cutting die-head, thread-rolling, and rib-strip-plus-roll, covering bar diameters 12-40 mm with 3-7.5 kW motors. Selection hinges on thread type (straight UNC vs tapered), production rate, and bar diameter, with tapered threads cuttin

Electroslag pressure welder installation for vertical rebar splicing on bridge columns requires a 380 V power feed, a welding head sized for 16-40 mm bar diameters, and a verified arc-to-upset timer sequence per JGJ 18-2012 or AWS D1.4, with plate ESW restricted on US fracture-critical members per F

Walk-behind and ride-on power trowels need a controlled unboxing-to-startup sequence: handle assembly, engine/fuel check, blade pitch verification, and a 60-90 second no-load run before the slab. Blade selection by machine model is the most common install-time failure, mapped by 22 OEM fitment chart

For power trowels, acquisition runs 20–40% of lifecycle cost while operating, maintenance, and downtime carry the remaining 60–80%; concrete-finishing fleets planning 2026 spec changes should model the 7-component TCO framework to expose hidden 3–9x unplanned repair penalties.

Electroslag pressure welders split into two distinct machine families that engineers still confuse: portable rebar EPW heads (16-40 mm bar, axial upset) and plate ESW gantries (30+ mm plate, wire-fed, no upset). Selection hinges on bar diameter range, current rating, upset force, and code path: AWS

Pneumatic (air) impact wrenches are classified by drive size from 1/4 in to 3-1/2 in, by handle style (pistol, D-handle, rod/lever), and by hammer mechanism (twin, jumbo, pin, pinless). 1/2 in and 3/4 in drives dominate auto and plant maintenance, with torque up to ~3,000 ft-lbs for 1 in+ drives.

Sander total cost of ownership (TCO) is a 5- to 10-year lifecycle model that converts purchase price into a comparable cost-per-finished-unit metric, weighting abrasive media, power, dust extraction, labor, and consumable changeover. For a 1,500 W random orbital sander running two shifts, abrasive a

Stud welding attaches a fastener to a base plate in a fraction of a second without drilling, threading, or filler metal, but it is unsuitable for high-strength structural steel, stainless steel, and high-alloy grades. Throughput reaches 60 studs per minute on CNC cells, and limitations are equipment

Pneumatic nail guns fire fasteners via compressed air, deliver the fastest cycle times, lightest hand-weight, and the lowest per-shot cost for high-volume framing, but tie the operator to a compressor + air hose, limit fastener length (commonly capped at 3.25 in on some cordless-look-alike Paslode-s

Pneumatic nail guns are the dominant class of fastening tools on jobsites, driven by compressed air at 70-120 psi and classified by fastener type, angle, and application. The main sub-types include framing, roofing, siding, flooring, brad, pin, finish, and palm nailers, each matched to a specific fa

Demolition hammers split into three drive families (pneumatic, electric, hydraulic) and three handheld weight classes (5-10 kg, 10-15 kg, 15-30 kg+), plus carrier-mounted breakers above 30 kg. Selection hinges on chisel shank, impact energy, vibration control, and indoor-versus-outdoor power logisti

Hand-held 110–125 mm marble cutters install in 30 minutes on a 220–240 V single-phase outlet with RCD protection, while 22 kW bridge saws and 75–90 kW block cutters demand a 380 V three-phase feed, 4–20 m³/h water supply, and a 6.0×5.0 m footprint. Match blade, motor wattage, and dust extraction to

Marble cutters fall into three primary power classes: electric, pneumatic, and hydraulic, with blade type (continuous rim, segmented, turbo) driving cut quality. Selection hinges on motor wattage, no-load RPM, blade diameter, and wet vs dry duty. A 4-1/2 inch (115 mm) electric cutter is the baseline

Circular saws deliver portable, fast cuts across wood, metal, and masonry, with blade swaps covering rip, crosscut, and bevel work. Trade-offs include limited depth-of-cut versus a table saw, lower precision without a fence, and kickback risk on handheld passes. Corded 15 A sidewinders start near $1

A circular saw's true cost of ownership spans purchase, installation, energy, blades, consumables, maintenance, downtime, and depreciation, with the recurring 5-10 year envelope often exceeding the headline price. ProcurementIQ rates circular-saw TCO as Low overall, while SkyQuest projects the blade

Cut-off machines divide into two main classes by cutting medium: abrasive-wheel power cutters (chop/miter, swing-frame, pendulum) for metal, masonry, and castings, and toothed-blade machines (cold saw, flying rotary-linear, milling) for steel pipe and tube. Selection is driven by workpiece material,

Impact drills (冲击钻) are classified as mid-power rotary tools sitting between hand drills and rotary hammers, with two impact mechanism variants: dog-tooth and ball-type. They are specified for masonry, brick, and light-concrete drilling, and for driving fasteners when clutch-controlled torque is acc

For bridge construction, an oxy-fuel cutting torch sized to the thickest plate, matched seat type, and the right fuel gas (acetylene for 10-20 mm or propylene for thicker structural members) is the decisive spec. Equipment cost stays at $250-$350 for a full rig, and mild steel up to 12 in (300 mm) i

For landscaping steel work, an oxy-fuel cutting torch with acetylene or propylene fuel and a tip rated to 3/4 in. mild steel is the practical entry point, using mild-steel-only selection rules and 1,600–1,800°F ignition logic.

For electrical-installation work, an oxy-fuel cutting torch is selected by seat type, metal thickness, application, and fuel gas; acetylene (5,600–5,800°F flame) suits thin detail cuts, propane/propylene suits stable field work, and 3–300 mm mild-steel thickness is the practical cut window.

An oxy-fuel cutting torch sized to 1/8–3/8 in. (size 0/00 tip) or 1/2–3 in. (size 1–3 tip) mild steel, run on acetylene at 5,600–5,800 °F flame, with reverse-flow check valves and a seat type matched to the torch brand, is the baseline spec for plumbing-installation pipe and hanger work.

Oxy-fuel cutting torches are not specified for masonry; they cut carbon and low-alloy steel up to 12 in thick. For concrete, brick, or stone, the right tool is a diamond-blade saw or a hydraulic splitter/pulverizer, with the torch reserved for exposed rebar.

For demolition work, specify an oxy-fuel cutting torch by material thickness, joint accessibility, ignition-source constraints, and reach, with acetylene for fast preheat and propane for robust field availability. A 36 in. heavy-duty straight torch keeps operators away from heat and slag; thicknesse

Oxy-fuel cutting torches for interior finishing work typically pair an acetylene fuel gas with a 3 mm to 300 mm tip range, a 5,400 to 5,800 F pre-heat flame, and reverse-flow check valves for indoor flashback safety. For ductwork, stair fabrication, and shop-floor trim cuts, a medium-duty outfit (e.

Oxy-fuel cutting torches remain the lowest-cost, most portable option for road-maintenance steel work, with selectability driven by four gates: seat type, metal thickness (3 mm to 300 mm mild steel), application profile, and fuel gas. Acetylene gives the fastest preheat at 5,600 to 5,800 F, while pr

Oxy-fuel cutting torches remain the workhorse for carbon-steel construction, with hand torch kits covering 3 mm to 300 mm mild steel using acetylene preheat at 5,600–5,800 F. Selection is driven by four gates: tip seat type, plate thickness, duty class, and fuel gas compatibility with downstream cos
Standard oxy-fuel cutting torches only sever steel cleanly, and on concrete jobs they reach the rebar by first cracking the matrix with a pulverizer or splitter. Exothermic rods, plasma, and hydraulic shears each cover the edge cases where open-flame oxy-fuel is wrong.

Bridge construction and rebar-prep work pulls plasma cutters into a thickness band of 0.5–50 mm mild steel with cuts of 6–25 mm structural plate typical. A 60–80 A inverter at 100% duty cycle covers 1/4" to 3/4" plate, with CNC and HF pilot arc matching field rebar and stiffener cuts.

Tunnel construction needs a 60–130 A plasma system with at least 60% duty cycle at 40 °C, IP23S enclosure, and CNC-ready arc-start logic. Handheld 40–50 A units are suitable only for rebar trim and utility crosscuts, not primary structural cutting.

Landscape fabrication work (gate frames, planters, fire-pit rings, rebar assemblies) needs a 30-50 A dual-voltage plasma cutter with 1/4-1/2 in mild steel clean-cut capacity and a 60% duty cycle, matched to a portable 110V/220V supply and a 4-6 CFM compressor.

For HVAC installation, a 20-30A pilot-arc plasma cutter with 120V/240V dual-voltage input, 4-5 CFM @ 90 PSI clean dry air, and at least 35% duty cycle is the spec sweet spot for 26-16 gauge ductwork, with a 20-30% amperage headroom over typical 1/8"-3/16" mild steel cuts.

For electrical installation work, a 40–60A dual-voltage (120V/240V) inverter plasma cutter with at least 60% duty cycle and 5–6 CFM of clean, oil-free air at 60–90 PSI covers 1/4 in to 1/2 in steel bracketry and conduit supports; buy 20–30% more amperage than your typical plate to keep dross low and

For plumbing installation, pick a plasma cutter by pipe material and wall thickness first, then voltage and amperage. 110/120V inverters handle up to ~1/8 in. clean cuts on mild steel; 220V units reach 1/2-5/8 in. clean and ~1 in. severance. Compressed air must stay clean and dry at 60-72 PSI for pi

Demolition-grade plasma cutting is defined by 65–125 A output, 7.6–8.3 bar clean dry air, and 50% duty cycle at full amperage; matching these gates prevents the most common site failure modes.

For interior finishing work, a 30–50 A dual-voltage inverter plasma cutter on 60–90 PSI clean dry air at 4–6 CFM covers sheet-metal, HVAC duct, and light fabrication up to ~10 mm clean cut, while 60 A+ units with pilot arc are reserved for steel stud and thicker plate runs.

For road maintenance crews cutting guardrail, sign post bases, and patch plate up to 5/8 inch mild steel, a 40 to 45 A inverter plasma cutter at 120/240 V dual voltage, 50 to 60 percent duty cycle, and 5/8 inch rated edge cut, paired with a clean compressed-air supply at 6.0 to 7.0 bar, is the field

For steel construction, pick a plasma cutter by everyday plate thickness, not maximum rating: 25-45 A machines cleanly sever up to 5/8 in mild steel, while 60-80 A units handle 1 in plate at production speeds. Match duty cycle (50-100% at rated output), input voltage (110 V vs 220 V single-phase), a

For tunnel construction in 2026, pick an AC/DC pulse TIG welder with 250-400 A output, water-cooled torch, HF arc start, and 100% duty cycle, paired with a separate engine-driven unit for off-grid headings.

For landscaping fabrication, a 160-200A AC/DC inverter TIG welder running on 240V with at least 60% duty cycle covers steel edging, aluminium planters, and stainless irrigation frames in a single bench-side package. Skip the 110V entry-level units; they stall on 3mm plate common in landscape work.

For plumbing installation, a 160-210 A DC-capable TIG welder with HF start and fingertip amperage control matches stainless and carbon-steel tube work at 120/240 V dual input; AC is unnecessary unless the system carries aluminum. Pick a machine under 50 lbs with Dinse torch support and verify duty c

TIG is the wrong process for masonry, which is non-conductive: select a TIG welding machine by amperage, duty cycle, AC/DC type, and arc-start method, then size it to steel thickness, not to brick or block. Use 1 A per 0.001 inch of steel, add 25% for aluminum, and verify IEC 60974-1 duty cycle befo

For interior finishing work, specify an AC/DC TIG welder delivering 160-225A on 110/220V dual-voltage input, with HF start, pulse, and at least a 60% duty cycle at the working amperage. DC-only units are restricted to steel and stainless; aluminum trim requires AC. Foot-pedal amperage control and po

For road-maintenance TIG work, an AC/DC inverter with HF start, 200–350 A output at 40–60% duty, and a water-cooled torch above 200 A sustained is the defensible spec, matched to joint thickness and base metal. Road crews welding patching plates, crack repairs, and sign/gantry steel should size by t

For structural steel fabrication, specify an inverter DC or AC/DC TIG machine at 200–375 A with 40–60% duty cycle, HF arc start, and 99.99% argon shielding, matching the thicker base metal via the 1 A per 0.001 in. rule. Pick water-cooled torches above 200 A sustained and prefer AC/DC for shops hand

For bridge construction, the right arc welding machine is an engine-driven dual-arc generator in the 380-800A class (15-35 kW auxiliary), selected to AWS D1.1/D1.5 and JT/T 722-2023 with FCAW/SAW/GMAW process support for 25-80mm plate work and sub-zero preheat capability.

For HVAC installation, choose a 120V/240V dual-voltage multi-process arc welder with 200-265A output, 25-30% duty cycle at rated current, and verified input plug/breaker compatibility to handle sheet-metal ductwork, hangers, and on-site repairs in a single package.

Arc welding machine selection for electrical installation is a four-number spec exercise: input voltage and phase, rated input current, open-circuit voltage, and duty cycle at a stated welding current. Match those to the cable run, breaker, and electrode class before buying, otherwise the install fa

Plumbing-installation arc welders are commonly selected in the 130–250 A range for stainless and carbon steel pipe, with TIG (GTAW) specified for cleanliness on potable and process lines and MMA (SMAW) stick for field tie-ins. Verify electrode polarity, thickness envelope (≥0.25 in/6.35 mm), and dua

For demolition work, a 250-400 A DC inverter stick (SMAW) welder with at least 60% duty cycle, 3-phase input, and 4.0-5.0 mm electrode capability is the standard 2026 selection, balancing portability around 21 kg and field-tolerance for dirty cut steel.

For road maintenance, a 220 V single-phase inverter MMA welder in the 200–400 A bracket with 60% duty cycle at rated output is the default 2026 pick; engine-driven units are reserved for sites without grid or generator power.

For concrete work, arc welding machine selection pivots on five spec gates: process family (typically MMA/stick for rebar ties, SAW for prefabricated cage lines), output amperage, duty cycle at 40°C, input supply, and electrode diameter. Match the 220 V single-phase portable inverter (US$34–597) for

For bridge construction, aluminum crossover/bridge ladders with 6063-T5 or 6082-T6 alloy, 150 kg working load, and EN 131 / ISO 14122 compliance are the default pick. For vertical pier access, EN 131 single straight ladders in 2-6 m lengths at 390 mm width cover most spans, while 0.45/0.75 m wide la

For tunnel construction, specify Type IA (300 lb) or Type IAA (375 lb) aluminum ladders in 6061-T6 extrusions with 1.2-1.6 mm rail wall, 30 x 30 mm box rungs, 150 kg EN 131-2 rating, and a fall-arrest post; match alloy temper, working height and joint type to confined-space access rules.

Aluminum 6063-T5 single straight ladders sized 2-6 m, 150 kg rated, EN131-tested, are the practical pick for routine landscaping access; a multi-purpose or wheeled PIR platform suits higher-reach tree and hedge work above 5 m.

Fiberglass-reinforced plastic (FRP) ladders are the safer default for live electrical installation work because aluminum conducts current, but aluminum step ladders remain acceptable for de-energized or low-risk tasks when 6063-T6 construction, EN 131 or ANSI A14.2 ratings, and non-conductive rubber

For plumbing installation work, an EN131-rated aluminum step or single straight ladder in 6061-T6 or 6063-T5 alloy, sized 2.0–4.0 m with 150 kg SWL and 75° lean, is the standard pick; pick fiberglass instead for any work above 1 kV overhead lines.

Aluminum ladders remain a defensible choice for low-risk, short-duration demolition access, but ANSI Type IAA fiberglass substitutes are specified where hidden live utilities or welding slag are present. The selection hinges on duty rating, material conductivity, and the 9 m UK rest-platform trigger

For interior finishing work, an 8 ft aluminum Type II step ladder (225-300 lb load) fits ceiling-fan, crown-moulding, and drywall tasks; for fixed access, custom 6061/6063 extruded rail-and-rung profiles or steel-frame ladders with ribbed aluminum anti-slip steps serve better.

For steel construction, aluminum ladders in the 6063-T5 and 6061-T6 grade band ship in 1-6 m lengths at 150 kg rated load, with 63x24 mm stiles, 30 mm anti-slip rungs, and EN131/ANSI A14.2 conformance; pick a scaffold-fixed vertical ladder for permanent steel-frame access, an A-frame step ladder for

ZLP500–ZLP1000 suspended platforms at 500–1000 kg rated load suit most landscaping access; choose 630 kg units with hot-dip galvanized or 316 stainless wire rope for vegetation, and 800 kg models with VFD hoists when working height exceeds 100 m.

For plumbing installation on building exteriors, a ZLP-series two-point electric suspended platform (2-7.5m deck, 250-630kg rated load) sized to a 2.0 safety factor and 1.5m/s wind-cutoff is the baseline spec, with multi-point or stainless-rope variants required above 50m or in coastal sites.

Suspended platforms for masonry are split between low-rise hydraulic work platforms (e.g. LISSMAC MAB 1201, 1,200 kg, 0.48-1.99 m lift) and rope-suspended two-point swing stages rated 500-1,000 lb for facade work above mid-rise heights. Selection turns on building height, roof rigging feasibility, a

Suspended platforms with 30 kN safety locks and 1.5–3.0 kW hoists (ZLP630/ZLP800) match most demolition façades, provided the rig is anchored to structural members, not parapets, and wind limits stay below 12 m/s.

For interior finishing on mid- and high-rise façades, a ZLP630 or ZLP800 temporary suspended working platform (500–800 kg rated load, 1.5 kW hoist, 8–10 m/min lift, EN 1808 / GB/T 19155) is the practical baseline; narrow interior atrium work drops to a 1.3 m module on a parapet rig, while stone-clad

For road-maintenance access, select a suspended working platform by matching the ZLP-class width, rated load, hoist power, and rope spec to the actual work, not to the deck price. Roads split into bridges, tunnels, retaining walls, and noise barriers, each pushing a different load, height, and geome

For steel construction, ZLP630 and ZLP800 suspended working platforms are the typical pick: 6mm wire rope is sized for loads up to 400 kg, while 8 mm rope covers 400-800 kg with a 30-50% service-life gain from monthly lubrication.

For concrete work, choose a suspended working platform by matching platform length, hoist power and rated capacity to the elevation and crew load. Modular 1.5-6 m decks, twin 1.1 kW hoists, 500 kg rating, 14° tilt limit, 10 mm 6×19 wire rope and Cap. 59I compliance frame the 2026 spec window.

Climbing formwork selection for bridge construction pivots on pylon height, repetition count, and crane availability. Crane-lifted jump form suits pylons under 60 m with ample crane time; hydraulic self-climbing systems dominate above 80 m and where Level 5 wind tolerance or narrow shafts apply. Bri

Crane-climbed jumpform suits HVAC installations up to about 30 storeys where the mechanical risers are tied to the structural core; self-climbing systems win above 40 storeys and on tight crane-share sites, with PERI ACS Core 400 cylinders rated at 40 t and Doka SKE50/SKE100 at 5 t and 10 t respecti

Climbing formwork selection for electrical-installation scopes is dominated by wall geometry, pour height and crane availability, not panel colour. Crane-jumped systems suit cores under 80 m, hydraulic ACS owns the territory above 100 m, and cantilever single-sided platforms handle lift-pour cables

Bridge construction scaffolding selection hinges on matching system type to span, load, and access geometry: cuplock for piers at 75 kN/leg, H-frame falsework for 5-15 m deck pours at 25 kN/sqm, movable scaffolding systems (MSS) for repetitive segment casting, and ringlock for curved or variable-ele

Tunnel scaffolding selection hinges on matching the system (cuplock, ringlock, hydraulic traveller, cut-and-cover gantry) to ground pressure, span, and load: wet concrete 20-50 kN/m², deck falsework 25 kN/m², pier legs 75 kN minimum, with 1.6 safety factor per IS:875.

For electrical installation work, fibreglass (FRP) scaffolding is the only material that combines structural capacity with full electrical isolation, per April 2026 guidance. Steel and aluminium towers are common but conductive, so selection must balance tower class, plank spec, and proximity t

For plumbing installation, pipe clamp scaffolding with 48.3 mm OD, 3.2 mm wall EN 39 / S235GT tubes, OSHA-compliant guardrails, and base-jack leveling is the dominant choice on complex pipework sites in 2026, because it adapts to overhead, parallel, and crossing pipe runs that prefabricated frames c

Masonry scaffolding selection hinges on three gates: working height (≤10 floors vs 10–30 vs >30), live-load class (≤3 kN/m² light masonry vs >3 kN/m² heavy), and frame geometry (walk-through arch vs step/ladder). Q235B main frames with 42×2.5 mm verticals at 1219 mm width dominate export-grade specs

Demolition scaffolds must be heavy-duty to AS/NZS 1576.1:2019, erected to full structure height, anchored with torque-verified fixings (chemical anchors proof-loaded at 1.25x working load), and selected for debris containment rather than just access.

For concrete work, scaffolding selection turns on three numbers: pour height, slab live load (typically 2-5 kN/sqm for slabs, 5-7.5 kN/sqm for heavy formwork), and prop extension range. Match steel push-pull or telescopic props sized 2.2-4.0 m or 3.0-5.5 m to the pour before choosing system scaffold

For bridge construction, a Class II 635-650 nm self-leveling line laser with ±1.5 mm accuracy, 15-30 m working range, IP54+ housing, and matched pulse detector covers most deck and pier layout tasks; green 510-532 nm units win only above 500 lux ambient at 1.5-2× cost.

For tunnel construction, an infrared line level with 1,000 ft (305 m) minimum detector range, IP66 sealing, and dual-axis ±5° self-leveling is the workhorse pairing with a heavy-duty elevating tripod. Green rotary (515-532 nm) wins for heading visibility, but IR/red line modules fit formwork and seg

For landscaping layout in 2026, infrared line levels in the $23-$54/pc FOB-Ningbo band suit machine-vision and sensor-driven alignment, but visible green cross-line lasers at 510-532 nm remain the correct tool when a human reads the line on grass, soil or paver beds under daylight.

For HVAC installation, specify a 635 nm or 660 nm visible reference line plus a co-aligned 850 nm or 940 nm IR channel, with ±0.2 mm/m accuracy, IP54 housing, and a matched line receiver for ceiling-grid and duct-alignment work above 10 m. Match laser class to IEC 60825-1 limits, since IR exposure c

For demolition crews, an infrared line level with 100-165 ft detector range and 30-40 ft naked-eye visibility in low light suits alignment of long cut lines, while an infrared emitter (not a level) handles heat-based coating and adhesive release. Spec by range, accuracy, beam color, and IP rating fi

For 2026 road maintenance, a green-beam line laser in the 515-532 nm band, ±0.3 mm/m accuracy, IP65 housing, and Li-ion power is the typical spec floor for asphalt patch, curb, and formwork layout. Above 30 m runs, pair with a matched green detector; the same unit is ineffective for stakeout above 5

For concrete layout work, pick a dual-emission infrared line level rated Class II at 635 nm visible plus a Class 1 850 nm or 940 nm IR channel, ±0.5 mm/m accuracy, IP65 housing, and 30–50 m detector range. Reject any spec sheet lacking a wavelength, IP code, and laser class. (2026-08)

Bridge construction demands laser distance meters that combine 100-240 m range on reflective targets, ±1.5 mm accuracy minimum, Class 2 eye-safe lasers, and IP65 drop-rated housings to survive outdoor placement and vertical-alignment workflows. A four-gate filter of range, accuracy, laser class, and

Tunnel construction laser distance meter selection is a three-class problem: 0.05-150 m handheld phase-shift units for face and lining checks, 3.5-5,000 m pulsed time-of-flight sensors for profile and convergence monitoring, and IP54/IP67-embedded modules for TBM integration. Match range, accuracy,

For landscaping measurement, choose a green-beam, IP54-or-better laser distance meter with 0.05–80 m range, ±1.5 mm accuracy, and a 360° tilt sensor; avoid indoor-only red units under $30 and any Class 3B+ pulsed tool meant for surveying.

HVAC installers in 2026 should pick a laser distance meter by worst-case duct run, not by headline range: a Class II 40-50 m IP54 handheld with ±1.5-2.0 mm tolerance covers 80% of interior fit-out work, while green-beam and 80-200 m units are required for plenum and rooftop layouts in daylight.

Handheld laser distance meters at 50 m with ±1.5–2.0 mm accuracy and IEC 60825-1 Class 2 output are the default pick for electrical installation layout, while ±1.0 mm IP65 industrial units cover switchgear rooms and 0.1 mm triangulation sensors handle sub-millimetre panel work.

For plumbing installation, pick a handheld laser distance meter with 30-50 m range, ±1.5 mm accuracy, Class 2 laser, and at least IP54 ingress protection. Add Pythagorean/indirect mode for ceiling-to-floor transfers, and budget roughly $40-100 for a mid-range pro unit that survives a 2 m drop.

For masonry, pick a handheld laser distance meter with at least 30 m range, ±1.5 mm accuracy, Class 2 laser, and IP54 or higher; the 50 m phase-shift units near $22–$40 cover most block and brick layout work.

For demolition work, a handheld laser distance meter with at least IP54, Class 2 output below 1 mW, 0.05-50 m range, and ±1.5-2.0 mm tolerance fits most layout and pre-cut tasks. A green 515-532 nm beam beats red in dusty sunlit conditions, and a 2 m drop rating matters more than maximum range on a

For road maintenance, a Class 2 green-beam laser distance meter rated IP65 with 0.05–150 m range and ISO 16331-1 ±1.5–2.0 mm tolerance is the practical floor; pulsed time-of-flight units above 150 m add legal and PPE overhead and are usually unnecessary.

For steel construction layout, a Class 2 phase-shift laser distance meter with 100–200 ft range, ±1/16 in (±1.5 mm) tolerance, and IP54+ housing is the practical floor; below that, readings cannot be trusted against steel tape, and above 200 ft the tool class shifts to pulsed time-of-flight with dif

For concrete work, pick an IP65, Class 2 green-beam laser distance meter with 50-100 m range and ±1.5 mm tolerance, paired with a rotary laser for elevation control on pours over 30 m.

Bridge construction theodolite selection in 2026 collapses to four engineering gates: 1″ to 2″ angular accuracy, 2000–3500 m EDM range, IP54–IP66 rating, and tilt-corrected absolute encoders. Match accuracy tier to span and tolerance, not to budget.
For tunnel construction in 2026, theodolite selection centers on 1″–2″ angular accuracy, IP65+ ingress rating, 2,000 m+ single-prism EDM range, and a tilt-compensated absolute encoder. Specifying 5″–6″ units on metro or shield drives is the most common procurement failure, because segment-uplift mon

For demolition work in 2026, the theodolite spec collapses to three gates: 5″–6″ angular accuracy for setting demolition lines and tracking wall plumb, a 200 m+ reflectorless EDM to read targets through dust without a prism pole, and IP65 ingress protection for concrete slurry and rain. 1″–2″ units

For interior finishing, a 1 arc-second or 5 arc-second optical theodolite suits tight-tolerance partition and ceiling layout, while a construction sensor like the Leica iCS20 or iCS50 is faster for laser-projected MEP and drywall mark-ups. Choice hinges on room size, line-of-sight, and whet

For steel construction, theodolite selection hinges on angular accuracy (2" to 10"), IP54 weather rating, and 30x magnification with erect image, matching tasks like column plumb and anchor-bolt layout per theodolite reference data.

For concrete form alignment, anchor-bolt positioning and steel-column erection, a 2 arc-second digital theodolite is the practical accuracy floor; units like the Spectra DET-2K, Nikon NE-100, Nivel DT-2 and South NT-023 cover the 2-second to 10-second tier that contractors actually buy in 2026.

For bridge construction in 2026, automatic level selection hinges on three tool profiles: optical automatic levels for vertical control benchmarks, dual-grade rotary lasers for pier cap and deck drainage work, and PLC-driven 3D hydraulic leveling on bridge launching gantries. Spec the instrument to

For tunnel construction, an automatic level with 0.5 arc-second compensator accuracy, dual-axis tilt sensor, IP66 sealing and 1.5–3.0 km working range fits TBM segment ring alignment, NATM profile control and cross-passage transfer. Mount it on a TBM backup trailer with shock isolation; avoid high-v

For landscaping work in 2026, 24x to 28x magnification is the practical sweet spot for an automatic level: it balances target acquisition speed against optical clarity on sites under roughly 300 ft (90 m), while 32x is reserved for long-range grading tied to water-management grading rules.

Automatic level selection for HVAC installation hinges on Manual J load calculation, BTU capacity, and duct sizing, with four main system types: forced-air central, heat pump, ductless mini-split, and hybrid dual-fuel.

Automatic levels (self-leveling rotary lasers and optical self-levelers) give industrial electricians a ±1.5–3.0 mm/30 m accuracy envelope for conduit alignment, tray slope setting, and busway plane verification. Selection hinges on range class, IP rating, detector sensitivity, and power source matc

An automatic level is an optical surveying instrument with an internal compensator that keeps the line of sight horizontal, used by plumbers to set drain slopes, set fixture heights, and verify pipe runs across rooms. For plumbing work, 20x-32x magnification models with 1.5-2.5 mm/km accuracy cover

For masonry work, automatic levels (self-leveling optical, laser, and infrared) are selected by masonry type (CMU, brick, stone), required precision (1.5–3 mm/30 m), and job geometry, with rotary laser lines preferred on long bond runs and green-beam lasers favored indoors for visibility. L

An automatic level with an internal pendulum compensator is the default pick for road maintenance crews: setup drops to a single circular-bubble step, 1 km double-run closures of 1-2 mm are routine with mid-range 24x-32x instruments, and field acceptance is governed by ISO 17123 optical-survey toler

For concrete floor work, an automatic level choice comes down to the pour class: laser screeds with servo/laser receivers (typical ±1 mm flatness, S4–S5 slump) vs. self-leveling cementitious toppings (1/8 in to several inches) vs. trowel-applied resurfacing for thick repairs.

For bridge construction, choose a 0.5 arc-second robotic total station with sub-millimetric prism tracking and 1,000+ m reflectorless EDM range, paired with automated monitoring software that alarms on millimetre-level displacement 24/7. Manual total stations fit only short-span, low-risk layout wor

Robotic total stations with 1″ angular accuracy, sub-millimetre EDM, ATR prism lock, and IP65 sealing are the standard specification for tunnel construction. Selection pivots on five criteria: angular accuracy (0.5″–5″), range under dust/humidity, ATR lock speed, tunnel-specific software, and rugged

For landscaping projects under 1 acre, manual total stations at ±5 arcseconds and ±2 mm + 2 ppm distance precision remain the spec-to-price sweet spot, with robotic units justified only on sites with heavy staking. GNSS rovers lose line-of-sight games in tree canopy; total stations win wherever a pr

Robotic total stations such as the Leica iCON iCR70 and iCR80 give HVAC installers 1-person layout, sub-millimetre-to-3 mm angular accuracy, and direct BIM/IFC file import, making them the right pick for commercial ductwork, hanger, and MEP-coordination work where tolerances and schedule pressure do

Total stations for electrical installation are typically MEP-layout robotic instruments (Trimble RTS series) with 1-3 arcsecond accuracy, robotic lock, and indoor-class green or red beam lasers. Selection hinges on accuracy class, beam visibility, software compatibility, and tolerance to bright-ligh

For plumbing installation, total stations with robotic one-person operation, sub-centimeter accuracy, and BIM-compatible data flow deliver the strongest ROI; Trimble RTS and Leica iCON series dominate the MEP layout niche with proven field workflows.

For masonry layout in 2026, a 2" angular accuracy, 500 m reflectorless, 3500–5000 m prism-range robotic total station is the engineering sweet spot. Below 2" you overpay for tolerance the wall does not need; above 5" you risk bed-joint and verticality drift on multi-storey work.

For demolition work, total station selection hinges on dust/impact resistance (IP65+), reflectorless range to 1,000 m on concrete, and 2″ angular accuracy. Topcon's March 2026 statement confirms millimeter-grade accuracy is now achievable without a tripod, reshaping field workflows. Spec map co

For road maintenance, choose a robotic total station with 1-3 mm accuracy and automatic target recognition when continuous pavement deflection monitoring is required, or a manual total station for periodic as-built checks on a tight budget. Confirm the instrument covers the full sight envelope, with

Steel-construction layout crews need a robotic total station with sub-second auto-lock, 1-3 arc-second angular accuracy, and seamless GNSS hybrid handover to handle column plumb and splice alignment on jobsites from 1 to 30 storeys. Manual total stations still fit small bolt-up crews under 200 m rad

For concrete work, a robotic total station with 1-3 arcsecond angular accuracy and a green-beam auto-focus layout laser is the practical 2026 baseline; pick SPS-series for heavy civil, RTS-series for MEP/embed layout, and S-series when monitoring-grade precision is required.

Bridge construction layout demands dual-grade or single-grade rotary lasers with ±1.5 mm at 30 m accuracy, IP65+ sealing, and a Class 2 green or red beam, paired with mm-tracking receivers for grade match. Choose cross-line or 3×360° self-leveling units only for indoor formwork and rebar; avoid poin

Tunnel construction demands laser levels with at least 1,000 ft visible range, IP66 sealing, dual-axis self-leveling, and green-beam diodes for low-light heading work, paired with elevating tripods (3-8 ft) for vertical control. Shield segments lift when grout buoyancy exceeds code limits, so laser-

For landscaping grade work, a self-leveling rotary or 360-degree cross-line laser with green beam visibility and at least 100 feet of working range is the practical baseline; the HUEPAR HM03CG and DeWalt DCLE34020G both deliver 1/8–1/9-inch accuracy at 30–33 feet and IP54 site protection, fitting re

For HVAC installation, the right laser level is a 3-point dot or 3-plane green line laser with ±1/8 in or tighter accuracy, IP54 sealing, and 30-100 ft indoor range, matching duct slope, plumb, and ceiling-grid tasks. Rotary units are overkill indoors; cross-line only models fail on plumb transfer.

For electrical installation work, a green-beam cross-line self-leveling laser with at least ±3 mm at 10 m accuracy is the practical default; rotary lasers suit only large outdoor cable-lay or switchyard grading. Select by indoor/outdoor use, beam visibility, mounting, and IP rating.

For plumbing installation, a 3-point self-leveling spot/dot laser (e.g. DeWalt DW08302, 100 ft range, ±1/8 in accuracy) is the right pick over cross-line or rotary units. Green or red is fine indoors; pick red for budget, green for daylight visibility. IP54+ is mandatory on active job sites.

Green rotary and 3×360 cross-line lasers dominate the 2026 masonry market, with the Klein 93RLS winning the World of Concrete Industry Choice Award on March 12, 2026 and the HUEPAR 3×360 rated the best 360° model. For block and brick work, choose a self-leveling rotary laser for outdoor site elevati

For interior finishing in 2026, pick a self-leveling cross-line or 3D green-beam laser with accuracy between 1/32 in and 3/16 in at 30–33 ft, matched to room size and task; red-beam models suit budget DIY, while green 360-degree units dominate pro interior fit-out.

For road maintenance, a dual-grade rotary laser with receiver and ±10% slope range is the practical default, since pavement resurfacing, subbase truing, and drainage correction all need sloped reference planes across 200-2,000 ft radii. Pick IP66+ sealed units when milling or grading dust is present

Steel-structure erection demands rotary or multi-line green-beam laser levels with ±1/16 to ±1/8 inch accuracy at 30-100 feet, IP54+ rating, and detector support beyond 1,000 feet. For interior steel framing, 360-degree three-plane units like the Klein 93PLL (91 ft, green) or DeWalt DCLE14221GB (150

Wet-mix shotcrete machines in the 20–40 m³/h class dominate bridge construction selection, with 40 m³/h units (Grandever DHBT40-11-82, Saner 40 m³/h) delivering 15–16 m vertical reach and 11 MPa concrete pressure. Robotic arms suit pier caps; truck-mounted pumps handle deck soffits and abutments.

Wet-mix shotcrete pumps dominate metro and rail tunnel cycles above roughly 50 m³/h, while dry-mix rigs remain preferred for short repair and rehabilitation where mobility outweighs output. Selection should anchor on geology, target early strength, rebound control, hose diameter, and the machine's f

For landscaping shotcrete work, a 30–40 m³/h wet-mix shotcrete machine with a 15–16 m boom reach, ≤25 mm aggregate handling, and ≤10% rebound is the standard specification, sized from the 50–150 mm design thickness and total surface area.

For masonry strengthening, a wet-mix shotcrete machine at 8–15 m³/h with 0.4–0.6 MPa air pressure and 15–20 mm aggregate clearance is the default pick. Dry-mix rotor rigs (3–5 m³/h) suit small patch repairs; robotic arms (15–25 m³/h) suit large wall jacketing and seismic overlay work. Match output,

For demolition support and tunnel rehab, a wet-mix robotic shotcrete machine (30–40 m³/h, 7.5 MPa concrete pressure, 15 MPa–20 MPa main pump for long reach, 16 m boom) is the default choice in 2026; dry-mix rigs still suit confined one-off patches where compressor air, not pump output, limits progre

Interior finishing pools with sprayed concrete requires matching a shotcrete machine to shell geometry, hose diameter, and crew scale. For typical residential pools 30-50 ft long with 1-3 ft depths, a 3-inch hose wet-mix rig with 30-50 cu yd/h output balances mobility and rebound control.

For road maintenance work, pick a wet-mix or dry-mix shotcrete machine sized 5-15 m³/h with electric drive, matching output to the patch area and hose reach (35-200 m). Refuse any unit without documented rotor, seal and nozzle maintenance intervals.

Wet-mix rotor shotcrete machines in the 10-12 HP class, delivering 3-6 m3/h, are the practical default for steel-structure encasement and connection-pocket infill where rebound control and uniform density govern. Dry-mix units suit small, intermittent repair patches on steel members; wet-mix dominat

Wet-mix shotcrete pumps at 7.5-30 m3/h output fit most concrete work; dry-mix gunite rigs suit repair and refractory; match machine type, output, and mobility to the application.

Bridge deck and approach slab grinding needs walk-behind floor grinders in the 80–400 kg, 5–15 HP class, 720–880 mm working width, paired with M-class dust extraction. Edge perimeters and rebar cover work fall back to 115–230 mm angle grinders at 8,000–11,000 RPM.

Floor grinders for landscaping are walk-behind planetary or rotary units, 280-450 mm working width, electric or gas, used for smoothing concrete, removing coatings, and prepping stone, not stump or soil work. Choose by power source, head type, dust port, and diamond insert availability, then rent or

Spec a 1.5–3.0 kW single-phase planetary or rotary floor grinder with HEPA dust extraction for HVAC slab and duct-area prep, matching diamond grit 30/40# for coating removal and CSP 2–3 profiles per ICRI.

Single-phase 230 V brushless floor grinders now cover most UK electrical-installation sites, with three-phase 400 V reserved for sustained warehouse or industrial work. Match grinding width (18-22 inch residential, 25-30 inch commercial, 32 inch plus industrial) to project scale and head type to the

Floor grinder selection for masonry hinges on matching grinding width, head type, voltage, and dust control to substrate hardness and job scale. Planetary heads dominate polishing; counter-rotary gear-driven machines lead surface prep.

Floor grinders for demolition should match 80-100 kg walk-behind mass, dual-disc head geometry, and M/H-class dust extraction to the substrate hardness and coating type. Edco 2EC-NG-1.5 class machines and Hilti TE 1000/3000 AVR breakers cover coating removal and slab breaking respectively.

Floor grinder selection for interior finishing hinges on grinding width (18-22 inch residential, 25-30 inch commercial, 32+ inch industrial), planetary versus rotary head design, and project scale exceeding 1,000 sqm where ride-on or remote gear-driven units become economical.

For road maintenance in August 2026, select a floor grinder by mapping slab area, material removal depth, power supply, and head type (planetary vs rotary) to the cutting task. Use 18-22 inch walk-behinds under 1,000 sqm, ride-on planetary units above 1,000 sqm, and match diamond bond hardness to co

For steel construction site floor prep, a 32-inch+ planetary gear-driven floor grinder on 480V three-phase power is the right pick, with 18-22 inch single-phase units reserved for confined welder bays. Plan width, head type, power supply, and dust extraction against slab size, coating type, and FF/F

Floor grinder selection for concrete work hinges on three decisions: grinding width (18 to 22 in for residential, 25 to 30 in for commercial, 32 in+ for industrial), head type (planetary for polishing, rotary for coating removal), and power supply (single-phase 220V vs three-phase 220V vs propane).

For tunnel construction, concrete groove cutter selection hinges on matching cutter class to rock strength, vibration limits, and groove geometry: walk-behind diamond-blade saws for shallow utility slots up to ~80-120 MPa rock, rock milling cutter attachments on excavators for low-vibration profilin

For HVAC concealed-pipe routing in concrete and brick, a 110V, 1700–4800 W wall chaser with twin parallel 125–133 mm diamond blades, adjustable cutting depth, dust port, and soft-start is the current go-to spec band. Match voltage and amperage to site distribution, depth to pipe OD plus 10 mm cover,

Select a concrete groove cutter for electrical conduit work by matching power class, blade spacing, depth range, and dust extraction to the wall material and conduit diameter. Dual-blade wall chasers with adjustable 5–35 mm depth and 110V or 230V brushless motors dominate 2026 site practice.

For plumbing installations, pick a dual-blade wall chaser rated 1500-4800W with 0-40 mm depth, 8-42 mm width, 125-133 mm diamond blades and water-assisted dust control, matched to pipe OD and wall material.

Concrete groove cutters for interior finishing pair a hand-pushed groover with a wall chaser, sized to 1/4" edger radius, 4"x6" margin trowel work, and dust-controlled dual-blade channels for concealed conduit.

For 2026 road maintenance, the right concrete groove cutter matches blade width, depth control and power source to the contract spec. Walk-behind gasoline units dominate 31.0% of the category, with 5-10 mm grooves at 38.0% of demand. Iowa DOT requires 1/8-3/16 inch diamond groove depth on concr

For steel-construction contractors, selecting a concrete groove cutter is driven by blade diameter (14–16 in / up to 400 mm), cutting depth (4–5 in / 100–150 mm), power (5–7.5 HP electric) and water-cooling, with diamond blades the only practical choice for reinforced decks. Electric hand-push model

Bridge deck and approach-slab pours need ride-on laser screeds with 3-4 m vibration width, 100-500 mm leveling thickness, and grade-programmable heads; truss screeds fit narrow box girders. Key specs: engine 22-86 hp, travel 0-8 km/h, slope accuracy around 1-2 percent.

For tunnel concrete placement, ride-on laser screeds in the 35.5-63.9 kW class with 3.1-4.0 m vibration width and 100-500 mm leveling thickness are the practical spec envelope, paired with 2D sonic/averaging control since GNSS is denied underground. Compact walk-behind units (22 kW, 2.5-3.0 m) only

Two-wheel walk-behind laser screeds handle landscaping pours up to roughly 1,500 m²/day, while ride-on and 3D-guided models suit warehouses, airports, and ports above 5,000 m². Select by working width, paving capacity, F-number target, laser-control accuracy, and service access, not list price.
Impact drills deliver 13 mm masonry capacity at 600 W and 2800 rpm no-load speed; sanders cover orbital, belt and drywall formats. Cordless 18 V platforms now standardise both categories side by side.
For electrical-installation channel cutting and box-pocket chiseling, a 1,500–1,700 W SDS-max or hex demolition hammer in the 11–20 J class (1,500–1,900 BPM, 23–25 lb) is the spec band that matches 90% of conduit, junction-box and underfloor-tray work. Below ~1,200 W the operator burns motor time on
Plasma cutters handle any conductive metal from gauge sheet to 50+ mm plate; oxy-fuel torches win on low cost and thick mild-steel cuts up to 400 mm but cannot touch stainless, aluminum or copper.

Walk-behind laser screeds with a 2500 mm self-leveling head, 50 Hz vibration at 500 N exciting force, and stepless 0–65 m/min travel are the mainstream pick for HVAC plant-room and warehouse floor pours in 2026, sized by slab area, finish tolerance, and headroom access.

Laser screed selection for electrical-installation flooring hinges on matching machine type, working width, and laser-control accuracy to the slab's FF/FL target. Walk-behind units suit pours under 2,000 m², ride-on and boom units cover 2,000-5,000 m² per day, and three-wheel or boom systems handle

Laser screed selection for masonry hinges on mapping project area, slab thickness, and FF/FL tolerance to drive type: walk-behind under 1,100 m², ride-on 1,100–4,600 m², boom-mounted above 4,600 m². ASTM E1155 FF 50/FL 40 is the common contract floor for random-traffic industrial slabs, and head typ
For interior concrete slabs in 2026, ride-on laser screeds fit medium-to-large warehouse pours while boom-type machines serve wide-bay logistics and walk-behind units handle narrow pours and repairs. Match machine class to bay width, required FF/FL tolerance, mix slump, and access; verify electro-hy
For road maintenance crews, a walk-behind laser screed is the correct tool on patches under 2,500 mm wide, while ride-on and boom machines are reserved for large industrial slabs. Selection turns on slab size, FF/FL tolerance, access, and engine certification, not brand alone.

Laser screeds use a laser-guided strike-off head to hit FF/FL floor tolerances of FF35/FL25 to FF50+ on warehouse and industrial slabs, with walk-behind units running 0-65 m/min, 2.5 m heads, and 50 Hz vibration. Selection turns on slab area, flatness spec, mix design, and power source: walk-behind
Bridge deck finishing typically calls for a ride-on power trowel in the 24-37 HP range with 1,910-2,350 mm working width, chosen for 3,000-10,000+ sq ft/hour productivity on pours above 5,000 sq ft. Walk-behind units still handle edges, piers, and patches.
Walk-behind power trowels sized 24 in, 36 in and 46 in are the dominant spec choices for landscaping-scale concrete work, with 36 in being the mid-size default for patios, sidewalks and small pads. Match rotor diameter, engine power and blade pitch to slab size, not crew habit.
For electrical installation slabs, pick walk-behind 24-inch to 36-inch electric or battery trowels under 3,000 sq ft, step up to 36-inch to 48-inch ride-on hydraulic units above 5,000 sq ft, matching FF/FL floor flatness targets and indoor emission rules.

Walk-behind power trowels in the 24-36 inch range are the default for residential slabs over 200 sq ft, with diameter, blade type, and bolt-pattern fit driving selection more than engine HP. This guide maps the 2026 replacement-blade market to masonry work.

Power trowels are finishing machines, not demolition tools; for slab removal, contractors pair them with demolition hammers and core drills. Selection for site prep hinges on rotor diameter, engine class, and float-shoe setup matched to the existing slab condition.
For interior slabs over 200 sq ft, walk-behind power trowels (24-48 inch rotors, 4-13 HP) handle the bulk of the work, while ride-on units (24-65+ HP, 3,000-10,000+ sq ft/hr) take over once the pour exceeds 3,000-5,000 sq ft. Blade geometry, pitch, and material (steel vs steel-reinforced poly) decid

Power trowel selection for road maintenance hinges on matching rotor diameter, engine horsepower, and blade stage to slab size: 24–36 inch walk-behinds cover small patches, while 30–60 HP double-rotor ride-on units handle warehouse and airport decks. Lubrication intervals and blade sequencing drive

Walk-behind power trowels with 24-48 inch rotor diameters fit steel-construction slabs under 5,000 sq ft, while ride-on twin-rotor units cover larger pours. Select by project area, blade type, and power source.

For bridge construction in 2026, internal immersion vibrators with 35.8-38.7 cc 4-stroke gasoline drives at 3500 RPM and 1.4 HP remain the default pick for rebar-dense piers, with needle diameter matched to reinforcement spacing and a verified radius of action.

For tunnel concrete work, internal (poker) high-frequency vibrators in the 12,000-17,000 VPM range with matched head diameter and electric or hydraulic drive deliver the strongest compaction on heavily reinforced sections.

Landscaping concrete vibrator selection hinges on matching head diameter (1–2.5 in.), VPM (8,000–14,000), and power source to slab depth; internal/immersion poker units fit most patio and footing pours, while surface screeds suit thin overlays and form vibrators serve tight vertical work.

Concrete vibrator selection for HVAC installation centers on matching shaft length, head diameter, and VPM to slab/footing geometry, with electric 1.5–3 kW internal models the default for indoor mechanical-room pours. Use external form vibrators where rebar congestion blocks internal insertion, and

Internal (poker) vibrators at 8,000-14,000 VPM with 1-2.5 inch heads are the default for electrical-installation concrete pours; high-frequency electric models (200 Hz, integrated inverter) match congested rebar and thin sections where external form vibrators (500-10,000 lbf centrifugal force) are p

Internal immersion vibrators with 1.0–1.5 inch heads running 8,000–12,000 VPM suit most plumbing backfill and slab penetrations, while cordless 18V shaft-driven units (e.g. Makita XVR02Z) handle small-diameter pipe-encasement pours. Select by head diameter vs pour depth, VPM vs rebar congestion, and

Masonry pours call for immersion (internal) concrete vibrators with head diameters matched to wall thickness and rebar spacing, powered by either 115V mains electric drives or backpack-style lithium-ion cordless kits. Selection hinges on head diameter, shaft length, VPM, and power source, not on the

For demolition work, concrete vibrators are selected mainly to assess existing compaction and guide breaker, crusher, or splitter choice, not to vibrate fresh pour. Internal (poker) vibrators 8,000-14,000 VPM and 1-2.5 inch heads dominate the assessment role, while hydraulic and electric external fo
Interior finishing pours demand small-head (25-35 mm), high-frequency (12,000-18,000 VPM) internal vibrators matched to rebar density, with vibrating screeds reserved for thin toppings. External form vibrators suit architectural panels and closed forms where a poker cannot reach.
For road maintenance slab and patch pours, an internal (immersion) concrete vibrator with a 1.5–2.5 in head, 8,000–14,000 VPM output, and shaft matched to pour depth is the correct choice; proper consolidation cuts entrapped air from 5–20% to under 2% and adds 5–15% compressive strength.
For steel-construction columns, walls, beams, and slabs, internal (poker) concrete vibrators remain non-negotiable even for S4 mixes; selection is driven by slump, rebar density, head diameter, and amplitude. A 32 mm high-frequency steel-pipe head running 200/240 Hz at 48 V three-phase is a workable
Internal (poker) concrete vibrators remain the default on most pour sites, but selection hinges on head diameter, VPM rating, power source, and the pour geometry. Match a 1-inch head to ≤6 in. depth, a 2-inch head to ≤18 in., and step up to high-frequency or external form vibrators for heavily reinf
For bridge construction electroslag pressure welder selection, match bar diameter (typically 16-40 mm) and UPSET force to JGJ 18-2012 or AWS D1.4, avoid the process on fracture-critical tension members, and use NGI-ESW only for non-FCM plate splices under FHWA guidance.
Mechanical rebar couplers are the default splice for bridge piers, decks, and seismic columns where lap splicing wastes steel and slows cycles. Selection hinges on bar diameter (12–50 mm), steel grade (Grade 60/500/550), thread type, and project seismic class, with ISO 9001 manufacturing and ICC-ES
For landscaping structures like retaining walls, pergolas, and planter piers, threaded rebar couplers in 14-40 mm diameters with 40Cr or 45# carbon steel bodies deliver 100% load transfer, outperforming lap splices in congested formwork and reducing steel use.
For HVAC installation, specify rebar couplers by bar size, grade, and connection type: parallel-threaded for new pours, upset-end for HRB500/high-grade bars, and pressed-sleeve where no threading is feasible. Match the coupler to ASTM A615/A706 grade, the equipment pad or equipment-household rebar c
Rebar couplers for electrical-installation concrete work are typically cold-pressed sleeves or upset-parallel-thread mechanical splices, with sizes covering #4 (13 mm) through #18 (57 mm) bar and base materials of 20# / 16Mn / 40Cr / 45# carbon steel. Specifying them requires bar grade, code-class,
Mechanical rebar couplers sized 12-50 mm replace lap splices in plumbing work for water/wastewater structures, with three mainstream types (parallel-thread, upset-forged, cold-pressed) chosen by bar grade, congestion, and code class. For plumbing, specify 40Cr or 45# carbon-steel parallel-thread cou
Mechanical rebar couplers in #45 medium-carbon steel splicing HRB335/HRB400 deformed bars from 16 mm to 40 mm deliver 100 percent tensile load transfer and outperform lap welds in congested masonry. Pick standard parallel, reducing, or right/left thread types by bar mobility and diameter match, not
Standard parallel-thread rebar couplers in #45 carbon steel cover 16-40 mm bar diameters at US$0.20-0.75 per piece, with upset-forged and cold-extrusion variants reaching 800 MPa tensile transfer. For steel construction, selection pivots on bar size, grade, joint position, and certification: ISO 900
Mechanical rebar couplers replace lap splices in congested concrete work, with selection driven by bar size (commonly #4 to #18), grade (Grade 60/420 to Grade 80/550), and whether the joint is Type 1 or Type 2 per ACI 318. The right pick cuts steel tonnage, eliminates lap length, and survives seismi
For tunnel construction, select a rebar threading machine matched to bar diameter (typically 16-40 mm), thread length (100-300 mm), and motor class, pairing it with rebar couplers (40Cr/45# carbon steel) for mechanical splicing in confined headings.
Rebar threading machines in the 3-6 kW, 380 V class with 100-1000 kg frame weight suit HVAC rooftop steel-frame and equipment-pad rebar runs when throughput is low to moderate. For HVAC work, prioritise thread-rolling parallel couplers over cut threads to keep bar fatigue and ductility within seismi
For electrical installation sites, select a rebar threading machine rated 380 V, 3-6 kW, CE certified, in the 100-1000 kg class, matched to rebar diameter and coupler material (40CR or 45# carbon steel). Auto upsetters fit high-tensile bar; manual presses suit repair work. Verify thread length (100-
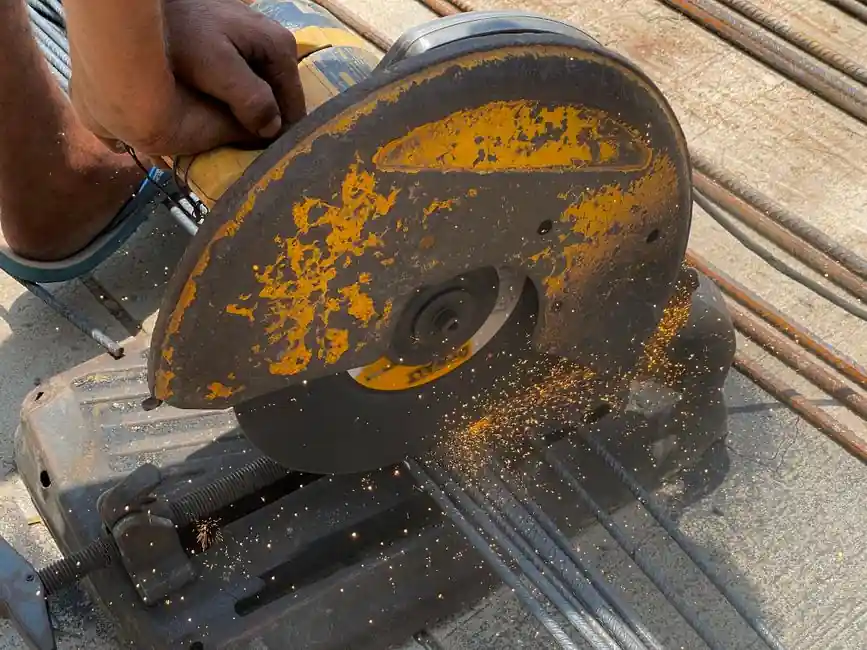
Rebar threading machines sized at 3-6 kW with 380 V supply and 100-1000 kg frame weight cover interior finishing rebar splicing; match thread length to coupler spec before choosing roll vs cut type.
For road maintenance crews splicing rebar on patch, bridge-deck, and barrier-repair jobs, the rebar threading machine that wins is a 380 V, 3-6 kW automatic thread-rolling unit handling 100-300 mm thread lengths on 40CR/45# carbon-steel couplers, with an upsetting machine and manual coupler press he
For 2026 steel-construction jobs, pick a rebar threading machine by rebar grade (HRB400/HRB500), diameter range up to 40 mm, 380 V 3–6 kW motor, CE marking, and thread-rolling versus cut-threading method. Spare parts, service coverage, and rebar coupler compatibility (per JGJ 107) drive total cost.
For 2026 concrete rebar splicing, pick a rebar threading machine by bar diameter range, thread length (100-300 mm), motor power (3-6 kW), and whether the line uses rolling, cutting, or upsetting-threading. CE-certified 380 V units at 100-1000 kg cover most site needs.
Bridge rebar straightener selection hinges on matching bar diameter range, yield-grade capability, and straightness tolerance to the project's primary reinforcement size and throughput target. For typical Grade 60 bridge rebar in the 12-32 mm range, horizontal four-roller powered straighteners at 4-
For tunnel rebar cages in 2026, a straightener sized to 12-32 mm bars at 8-25 m/min throughput, with servo pinch-roll control and a mandrel bend radius of 3-5d, is the working baseline. Match bar grade to coupler spec, not the other way round.
Plumbing installations rarely call for heavy rebar straightening, but where pipe supports, thrust blocks, and equipment pads embed deformed bars #3 through #6, a 1.5–3.0 kW portable straightener running at 4–6 m/min handles most site volumes.
Rebar straightener selection hinges on bar diameter range, yield grade, and production throughput. Match machine class to ASTM A615 grade 40/60 or higher, and verify straightness tolerance, motor power (1.5–7.5 kW typical), and mandrel rotation speed against your daily tonnage target.
For 2026 concrete rebar work, match rebar straightener capacity to bar diameter (D6–D40), motor power (1.5–7.5 kW), and bend radius to project scale, with hydraulic models serving civil and high-rise sites and portable electric units covering residential slabs. Spec gates now require bend-angle accu
Bridge construction rebar work typically pairs a 32mm class electric-hydraulic cutter for main bars with a 16mm cordless model for stirrups, with 1.5–3.0 kW power and hydraulic pressure above 60 MPa for steady #8–#10 rebar throughput.
Tunnel rebar cutting hinges on bar diameter, segment-cage volume, and jobsite power: hydraulic cutters up to #8 (25 mm) Grade 60 dominate segment yards, while TBM logistics constrain lighter cordless units in the bore. Matching cutter capacity to rebar stress bands documented for shield segments (ab
Landscaping rebar work shifts the cutter decision toward portability, dust tolerance, and small-bar-cycle speed rather than the tonnage of a fab yard. The 16-32 mm bar segment holds 43.0% of 2026 demand, so a battery or portable electric unit typically covers landscape edging, tree-anchoring, a
For HVAC installation, a 10-32 mm electric hydraulic rebar cutter covers most equipment-pad and concrete-anchor rebar work; pick a 1500-2200 W, 220 V single-phase unit with a 3-phase option for shop and a swappable blade set for on-site service. Match cutting capacity to the largest rebar on site, n
Hydraulic rebar cutters sized for rebar up to 32 mm diameter (e.g. HBC-232) typically cover most LV electrical-installation conduit and grounding-rod anchor work, while portable electric models handle 16-25 mm rebar on tight cable-tray sites. Match motor power (1.5-3.0 kW), cutting head force (15-30

For demolition work, specify a hydraulic rebar cutter rated for at least 25 mm bar stock with 380 V three-phase power, single-blade shear head, and a closed-loop blade-guard interlock. Demolition duty is the worst case for cycle life, so oversize by 30% over new-build sizing and verify spare-blade a

Rebar cutters for interior finishing jobs typically cover 10-25 mm (3/8 to 1 in.) diameters, with electric-hydraulic portables at 50-80 kg dominating indoor slabs. Choose by bar size, cuts per shift, and power source, not by max rating.

For 2026 road-maintenance rebar cutting, electric-hydraulic units cover #5 to #10 grade-60 bar (16 to 32 mm) at $275 to $2,399, with portable heads handling the field tie-in and dowel-bar work that defines pavement repair. Select on bar diameter, power source, and cutter-block availability rather th

Rebar cutter selection for steel construction hinges on matching the machine's bar-diameter capacity and power source to your heaviest rebar grade. Hydraulic and electric portable units cover #4 (13 mm) to #8 (25 mm) bar; for #9 (29 mm) and above, specify a hydraulic shear or a factory cut-and-bend

Hydraulic electric rebar cutters rated 4-25 mm at 1700 W dominate portable concrete-rebar cutting, with matched blade sets starting near $1.75 and 42 mm heavy-duty machines reserved for bridge and high-rise work. Match motor power, blade grade, and cutting capacity to rebar diameter and cycle time b

For bridge construction in 2026, size a rebar bender around the maximum bar diameter on the cage drawing (commonly 32-40 mm for pier and deck reinforcement), then validate power, bend-angle, and min-radius against the project's bar-bending schedule before procurement.

Tunnel-segment rebar cages for shield TBM drives stay in the elastic range at -80 to 50 MPa under construction loads, per Springer 2008 FE study; spec a rebar bender matched to segment cage geometry, bar diameter, and continuous-shift cycle time on 2026-08-10.

For landscaping work, the right rebar bender matches bar diameter (typically 10–16 mm) and bend-angle range to the application: manual units for one-off garden edging, electric portable units for repeated trellis or arbor bends, and higher-capacity machines only when structural concrete is in scope.

Electric rebar benders sized 10-42 mm diameter cover most electrical-installation conduit, grounding-rod cage, and substation-foundation rebar work. Spec the machine by bar grade, minimum inside bend radius, motor kW class, and site power, not by price alone.

For plumbing-installation rebar work, select a portable electric rebar bender rated for #4 (1/2 in) through #6 (3/4 in) Grade 60 bar at 90-degree bends, with a 110-220 V motor in the 1.5-2.5 kW range. A single-foot pedal, gearbox-driven bench unit typically runs 1,800-2,400 USD.
For masonry rebar work, select a portable electric rebar bender rated to at least 1" (#8) grade 60 capacity, with 110 V plug compatibility and a 180 lb carry weight, like the Fascut FS-600. Combo cutter-benders work below #6 rebar; dedicated benders are required for #8 and larger stock.

For demolition work, a rebar bender must double as a structural-steel cutter: portable hydraulic or cordless electric models cutting 16-22 mm rebar in 2-4 s suit bridge and slab demolition crews, while bench-mount electric benders with 32-42 mm capacity suit yard processing.

For interior finishing rebar prep, choose a rebar bender matched to bar diameter and bend angle: handheld electric for #4-#5 (10-16 mm), hydraulic bench units for #6-#8 (19-25 mm), and 42 mm-class machines only for structural tie-ins, never for partition or ceiling inserts.

For road maintenance crews, pick a rebar bender by rebar grade and diameter, motor class, and power source; #8 (25 mm) Grade 60 hydraulic benders dominate pavement and curb work, while 10–42 mm units fit bridge-deck rebar.

For steel-construction rebar bending in 2026, specify machine class by bar diameter: manual benders cover D10-D25 at 2.0-2.2 kW, portable hydraulic units reach D28-D32, and CNC integrated bender-cutters handle D40+ with 180 degree bends in roughly 5 seconds per cycle.
HVAC ductwork and bracket installation demands air picks in the 0.8-1.5 kW class, with hex shank 19-28 mm, BPM 900-1500, and ergonomic anti-vibration housings as primary selection gates.
Air picks for electrical installation should be sized at 10-20 kg class with 1500-2000 bpm striking rate, matched to a 0.6-1.0 m³/min portable compressor. Run at 5-7 bar dynamic line pressure, fit in-line lubrication and a moisture separator, and never substitute for cable-cutters on live conductors
Air pick (pneumatic chipping hammer) selection for plumbing installation hinges on matching piston bore, stroke, and blows-per-minute to pipe material and joint scale. Typical plumber-grade air picks run 0.4-0.8 kW at 90-120 psi with 1,500-3,000 bpm; avoid scaling up to demolition-class tools on cop

Air picks for demolition work are pneumatic hand tools sized by piston bore, stroke, blow frequency, and air consumption, with handheld classes typically 19-32 mm bore and 2-6 J per blow. Selection hinges on matching tool class to substrate (concrete, brick, asphalt) and matching compressor CFM/PSI

Air pick (pneumatic breaker) selection for road maintenance is driven by chipper weight class, blow frequency, and air consumption matched to the compressor on truck. Spec gates below compare 5-9 kg, 10-16 kg, and 17-30 kg classes against asphalt patch, curb, and bridge-deck tasks.

For bridge construction, specify 3/4" and 1" air impact wrenches delivering 600-1356 N·m (440-1000 ft-lb) at 90 psi (6.3 kg/cm²), 4500 rpm, twin-clutch, paired with a 1-1/2" ultra-heavy model (14.5-16.0 kg) for main girder bolts and 3/8"-1/2" ratchet-class tools for cabling trays.
Tunnel construction demands 3/4" or 1" drive air impact wrenches delivering 1200-2644 N·m torque on M27-M36 rock-bolt hardware, with twin-hammer mechanisms, 6.2-8.5 CFM air demand, and side-exhaust for confined heading air. Spec the drive and torque envelope to the largest bolt first, then verify ai

For landscaping work, pick 3/8" or 1/2" drive air impact wrenches in the 90-150 ft-lb nut-busting range, paired with a 3/4" option for auger and stump grinder fastener service. Air ratchet wrenches fit tight under-deck screw work, and garden machinery now ships with sockets sized for the chosen driv
For HVAC ductwork and condensing-unit bolting, a 3/8-inch drive air impact wrench in the 230-450 ft-lb (310-610 Nm) working torque range is the standard pick, with 1/2-inch reserved for line-set bracketing over 3/4 inch.

For electrical installation, pick a 3/8" or 1/2" drive pneumatic impact wrench in the 340-900 Nm torque band, 90-120 psi air supply, weighing 1.5-3.0 kg, with twin-hammer or pin-clutch mechanism, insulated composite or rubber grip, and side exhaust.

For masonry fastening, select a 1/2" drive air impact wrench delivering 600-1,000 ft-lb breakaway torque, paired with 3/8" or 1/2" air hose at 90 psi, twin-hammer mechanism, and 4-5 CFM air consumption at load.
For demolition work, 1-inch square-drive air impact wrenches in the 1,500-2,000 ft-lb nut-busting class are the practical floor; 3/4-inch models above 1,000 ft-lb cover most structural and automotive teardown, while 1/2-inch consumer-grade wrenches under 500 ft-lb should be excluded for sustained de

Air impact wrenches sized at 3/8" to 1/2" drive with 340-1,500 Nm max torque are the practical pick for interior finishing trim, cabinet, and drywall-fastener work; larger 3/4" and 1" units above 2,000 Nm belong on structural steel bolting, not finishing. Match torque, weight under 2.5 kg, and noise
For road maintenance, size the air impact wrench by the largest bolt the crew actually turns, not by the truck on site: 3/4" drive to ~1000 N·m covers most M16-22 hub and suspension work, while 1" drive (≈2000-2700 N·m) and 1-1/2" drive (14.5-16.0 kg class, FW-2700 type) are reserved for truck frame

For steel construction bolting, 1/2" air impact wrenches in the ~1,000 ft-lb class handle light structural work, 3/4" models cover A325/A490 field bolting, and 1" tools above 1,900 ft-lb are reserved for heavy erection. Match drive size, torque class, and bolt capacity to the joint, not the tool car
Air impact wrenches are not the right primary tool for concrete work; concrete fastening calls for rotary hammer drills or impact drivers with SDS-Plus shanks. A 1/2" pneumatic impact wrench rated ~550-746 N·m with twin-hammer clutch suits anchor-bolt snugging, not hole drilling.

Pneumatic nail guns for bridge construction require high-pressure framing or concrete-class tools (70-120 psi operating range), not light interior models; selection hinges on nail length, substrate, and duty cycle. Specification shortlists should match engineered fastener data to OEM pressure rating

Pneumatic nail guns are not the right primary fastener tool for tunnel construction: use rock drills, shotcrete anchors, or self-drilling rock bolts instead. A nailer only fits auxiliary timber formwork, dowel pinning, and temporary bracing, where a 14-gauge concrete T-nailer at US$31-36 FOB or an a

For HVAC installation, choose a pneumatic nail gun in the 70-120 psi operating range with a 2-3.5 inch fastener window, depth-of-drive adjustment, and a quick-clear nosepiece for sheet-metal-to-duct fastening on the jobsite.

For electrical-installation pneumatic nail guns, prioritize a sequential-trigger framing nailer (21° or 30°) at 70-120 psi, depth-adjustable nose, and dry-fire lockout, with contact-actuation banned on live conduit work. Coil nailers suit cable tray strapping; brad/finish nailers suit low-voltage pl
Masonry-grade pneumatic nail guns differ from interior trim tools: concrete-rated models start around US$45-55 per unit for entry-tier wholesale, while general-purpose guns cap at 0.8 MPa (8.3 bar) and are unsafe on masonry. Choosing the right tool requires matching substrate hardness, fastener type

Pneumatic nail guns are not the right primary tool for demolition; the correct demolition pairing is a chipping/breaker hammer or demolition hammer, with nailers reserved for temporary fastening, formwork, and selective strip-out. Key criteria: impact energy class (J), blows per minute, chisel vs ha

Pneumatic nail gun selection for interior finishing is driven by three matching decisions: nail gauge (18 vs 23), collation angle (0/20 vs 28-34 degree strip), and air-supply pressure around 3.5-4 kgf/cm squared. For trim, cabinet, and decorative woodwork, 18-gauge brad nailers and 23-gauge headless

For road maintenance pneumatic nail gun selection, prioritize the MAX CN-650M2 concrete/steel auto-feed tool (L=27-50mm, 0.8MPa max supply) over the SF5040 18Ga brad/staple unit (15-50mm, 100pcs mag, 8.3bar ceiling) by substrate hardness, nail length band, and duty cycle. Wood/template work uses SF5

For concrete fastening, gas-actuated and dedicated hardened-powder-actuated nailers outperform framing pneumatics; use 22-32 mm shank concrete pins at 80-120 psi (5.5-8.3 bar) on air models. Match tool to substrate, fastener, and duty cycle before price.

Stud welding is the standard process for attaching shear studs and anchor pins to bridge steel girders, with capacitor-discharge (CD) and drawn-arc (DA) machines dominating the two distinct on-site use cases. Selection hinges on stud diameter (typically 6–25 mm), base-metal thickness, and the applic

Concrete vibrator total cost of ownership spans power, shaft/hose replacement, and downtime over 3-5 years, not just purchase price. Electric plug-in models lead on energy and noise, gasoline units win on site mobility.

China-sourced concrete groove cutters on Alibaba and Made-in-China list in the US$400–1,500 FOB range per unit for diesel-engine models, with the deepest supplier pool concentrated in Zhejiang and Henan under OEM/ODM contracts.

Industrial power mixers are classified by mixing action (planetary, pan, twin-shaft, drum, continuous), drive power (electric, hydraulic, diesel), and shaft orientation (horizontal vs vertical), with motor ratings from 5.5 kW lab units to 250 kW+ heavy-industrial plants. Selection pivots on aggregat

Spring-rewind hose reels dominate industrial lubrication and compressed-air service, but picking the wrong drive or seal material is the single biggest source of field failures. Match the reel to media pressure, hose length, and mounting first, then validate against the manufacturer's selection guid
Air pick (pneumatic pick) installation hinges on a clean 6.3 bar / 90 psig dry-air supply, an FRL trio, and vibration-isolated hose sizing. Atlas Copco's pocket guide on air-tool installation underpins the four-step commissioning walkthrough below.
Chinese demolition hammer factories dominate the 2026 supplier map, with Yongkang/Zhejiang clusters producing 220V electric models from ~US$96/piece at MOQ 200 to 1500J+ hydraulic breakers for 6-9 ton excavators in the US$1,000-7,000 band.

Power mixers for road maintenance are selected on three loadouts: continuous mixers (3.5–5 cu yd/hr with 13 HP gas drive), power-auger systems for silo-fed mortar/stucco, and volumetric mobile mixers for mixed-on-site concrete under IDOT spec gates. Match drive, output, and water source to lane clos
Power mixers and cut-off machines serve different jobs: the first is an audio/editing software utility (PowerMixer v4.1, 70.02 MB), while the second is a 2000 W handheld abrasive saw with 355 mm blades at 3700 rpm. Spec them on use case, not on a single number.
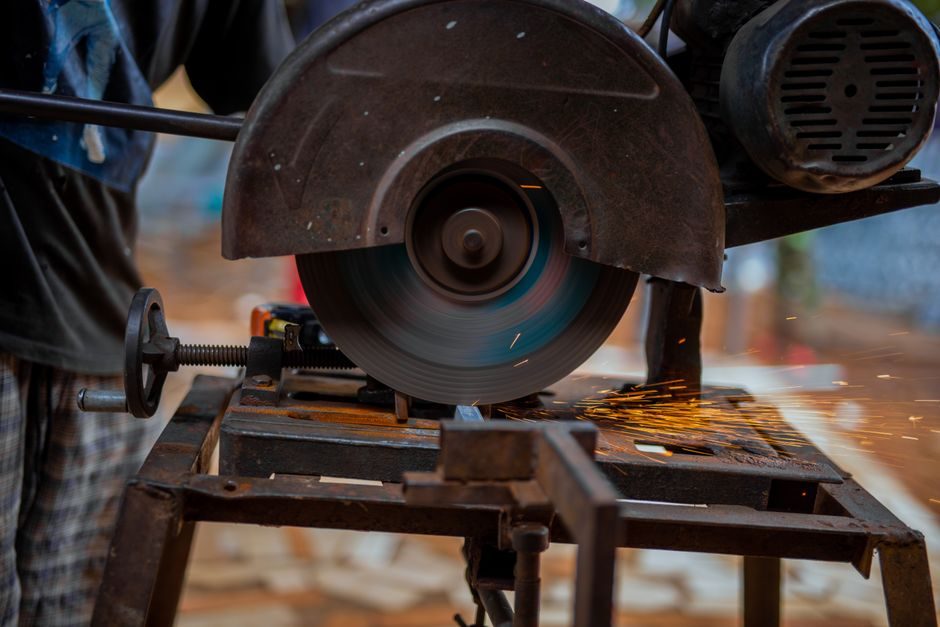
A stud welder and a circular saw are not competitors — they are complementary fab-shop tools. Stud welders join fasteners to base metal via arc or CD processes, while circular saws cut cold or hot-rolled stock. Selection between them is decided by job type, not specs.
HVAC duct and casing work demands a sander matched to sheet-metal gauge, joint compound, and substrate coating, with random-orbit and belt configurations sized to 80-180 m³/h airflow duct runs. Specifying by grit progression, dust class, and ATEX/IECEx zoning prevents the two most common installer f
Sander selection for electrical installation hinges on the surface profile needed on copper, aluminum, and steel conductors and enclosures, paired with IEC 60079 / ATEX dust-zone rules for any work on or near live hazardous-area gear. For panel work and busbar dressing, a 4.5–7 in. random orbital or

Demolition sander selection pivots on substrate hardness, abrasive cut rate, and dust class: match tool power (0.5–1.5 kW), pad diameter, and HEPA extraction to concrete, masonry, or adhesive removal per spec.

Sander selection for interior finishing turns on three axes: orbit size (3/32 in, 3/16 in, 3/8 in), power source (pneumatic vs brushless electric), and dust extraction. Pneumatic finishing sanders running at 90 PSI and 10,000-12,000 RPM dominate pro shops; brushless random-orbit wall sanders dominat

Sander selection for road maintenance hinges on matching machine class to surface type, application rate, and carrier hydraulics. Tandem, slipform, and broom units cover 2,500-12,000 m²/day on asphalt; drag-behind and zero-turn units serve 1-3 km/day on gravel shoulders. Pick by surface, throughput,

Sander selection for concrete work is driven by three variables: surface area, finish tolerance, and dust-control requirements. Orbital sanders fit detail and edge work; planetary and walk-behind grinders cover large slabs; matching abrasive bond and grit sequence to concrete hardness prevents rewor

For tunnel construction, a power mixer selection hinges on shotcrete duty cycle, muck-cycle integration, low-headroom geometry, and conformance to BS EN 16191. Twin-shaft compulsory mixers dominate segmental lining pours, while colloid and continuous auger units serve backfill grout and annular void

Selecting the right power mixer for a plumbing installation hinges on matching the mixer type to the material being blended, the batch size, and available power. For grout, mortar, drywall mud, or thin-set on a typical plumbing rough-in, paddle-style mud or mortar mixers in the 1.5–3.0 kW range are

Power mixers for demolition work must be matched to host carrier hydraulics (up to 350 bar / 300 l·min) and dust-control rules like OSHA's crystalline silica construction standard. Best-fit options: excavator-mounted processor power mixers (ALLU, 25-40 t carrier, 18,000 Nm drum torque) and standalon
For interior finishing, the right power mixer is a paddle-style mud mixer with 1/2 to 1-1/2 HP output, low-RPM torque, and a 115V brushless or cordless drive. Pick it by viscosity, batch size, and ventilation — not raw wattage.

For steel-construction concrete pours, the right power mixer pairs drum size and RPM to the structural element being cast: 260-500 L tilting-drum units (18-25 RPM) for foundations and slab work, 600-800 L (9 HP / 3 kW) for high-volume deck and column pours, with MDOT-style discharge-locking timing o
For landscaping demolition, match the breaker class to material: 11 lb electric hex/SDS-plus for flagstone and paver edges, 20-30 lb SDS-max for pool decks and boulder work, and 60 lb pneumatic or 38 lb/22 ft-lb electric for asphalt and reinforced slabs. Power source, chuck type, and impact energy—n

Demolition hammer selection hinges on matching impact energy (2 J to 62 J), chuck system and bit class to substrate. Heavy hex breakers dominate road and foundation work, while 12-28 J SDS-max class drives vertical light demolition. Pick by joules and bpm first, brand second.

For road maintenance, demolition hammers in the 1500-2000 W class with hex or SDS-max chucks and 30-65 J impact energy are specified for asphalt and concrete patch removal. Selection hinges on chuck type, blow count, vibration (m/s²), and power source matched to crew size and shift length.

For 2026 concrete demolition work, pick by impact energy (J) and chuck system, not wattage alone. SDS-plus suits 4-16 mm drilling and light chipping; SDS-max and hex 28-30 mm drive the 1,500-2,000 W breakers used on slabs and walls.

110 mm marble cutters with 1400 W motors are the workhorse pick for cutting wall chases, panel cutouts, and stone-ceramic gland entries during electrical installation. Selection hinges on blade match, no-load RPM, and dust-suppression design, not on raw wattage alone.
For masonry work, choose a marble cutter by matching blade diameter (110-125mm for trim, 350-450mm for slabs), motor power, and wet-cutting capability to the stone hardness and cut depth you need daily.

For demolition work, choose a marble cutter with 110-125mm diamond blade, 1200-1400W motor, no-load speed of 11000-13000 RPM, and a real demolition hammer rating rather than a tile-cutting model. CCC-certified 110mm 1400W units (e.g., model 6261A) sit at the entry tier; 1300W mini grinders are light

For interior finishing, pick a marble cutter by blade diameter, motor wattage, and dust management. Handheld 110-125 mm circular saws at 1200-1400 W handle tile and trim cuts, while rail-guided wet cutters at 1800-2400 W handle large-format slabs.
Marble cutters are not standard road-maintenance tools; a 115-180 mm handheld diamond-blade saw handles asphalt patch trimming and concrete curb cutting, while a self-propelled road saw fits full-width pavement work. Selection hinges on blade diameter, no-load RPM, IP rating, and power source match
For HVAC ductwork, sheet-metal, and plenum cuts, a 7-1/4 in corded circular saw with a 24-tooth carbide-tipped blade handles 26-gauge steel to 3/4 in plywood. Match blade tooth count, RPM, and dust extraction to the cut material, and pair with PPE rated for hot metal swarf.

For plumbing installation in 2026, the right circular saw is a 7-1/4 in cordless brushless model with a 24-tooth carbide framing blade, matched to pipe material and cut depth. Corded worm-drive or metal-cutting abrasive saws step in for cast iron and stainless.

Circular saws for demolition are high-torque, abrasive-rated machines built for cutting masonry, rebar-embedded concrete, and steel plate where reciprocating saws stall. Spec priority is blade diameter, RPM, motor wattage, depth-of-cut, and dust/water sealing rather than finish-cut precision.

For interior finishing, a corded 1200-1800 W circular saw with a 184-190 mm blade, 4500-5800 rpm no-load speed, and a TCT tooth count of 40-60 is the practical workhorse; blade choice and tooth geometry matter more than raw motor power for clean chip-free cuts in MDF, plywood, and melamine-faced pan
Concrete circular saws, not woodworking saws, are the spec path for road-maintenance asphalt and concrete cutting. Selection hinges on blade diameter 350-500 mm, wet-feed dust suppression, and 230 V or 3-phase power matched to the cutter's continuous-load rating.

Circular saws for steel construction are selected by matching blade diameter, tooth geometry, and RPM to material grade and section size. Cold-saw TCT and HSS blades dominate structural-steel work; abrasive wheels fit thin-wall tube. Specs to anchor decisions: 1400 W, 5500 r/min, 220-240 V (CS185A-2
Concrete-grade circular saws use 14-inch diamond or abrasive blades on 1500-1800W motors with wet-feed water pumps, priced US$169-1,350 per set on 2026 sourcing channels. Blade diameter, motor wattage, and wet/dry rating—not hand-tool class—define a proper concrete saw.

Impact drill selection for tunnel construction hinges on chuck size, BPM and torque ratings matched to rock bolt, anchor and utility-lining diameters, with SDS-Plus dominating handheld roles under 16 mm and SDS-Max or D-handle rotary hammers owning 18-45 mm work. Cordless 18 V platforms cover 80% of
Cordless 18V combi drills with 10 mm keyless chucks, 20+ torque stages, and 21,000+ bpm impact rates are the practical default for landscaping crews drilling wood, masonry, and light steel; corded rotary hammers are a better match for repeated 13 mm+ concrete anchoring.

For HVAC installation work, an impact drill must balance chuck size (1/2" for line-set brackets, 3/8" sufficient for thermostat boxes), torque (≥50 Nm for masonry anchors), and brushless motor durability. Match the tool class — corded hammer drill for concrete, brushless 18-20 V for steel stud — to

For electrical installation work, a 600W corded impact drill with a 13 mm keyless chuck and 210 mm depth stop covers 80% of on-site hole-drilling tasks. Pick chuck size to bit shank, match wattage to duty cycle, and verify insulation class before each shift.

For plumbing-installation work, choose a corded or 18–20 V brushless impact drill rated 60–80 N·m hard torque with 13 mm keyless chuck, dual-mode (drill + hammer), and a minimum 2-speed gearbox; the 12 V class is acceptable for ≤6 mm masonry anchors and copper-clip bracketing only.

For road-maintenance crews, an impact drill specified for concrete anchor and CFRP drilling needs 2.0 J minimum impact energy, SDS-Plus shank, and dual-mode (rotation + hammer) per TxDOT spec book. Cordless 18–20 V models suit ditch, sign-post, and bridge-deck tasks; corded 800 W+ units fit sho

For concrete work, choose an SDS-Plus hammer drill or rotary hammer (≥500 W, 0–2800 rpm, 13–25 mm capacity) over a standard impact drill when drilling holes above 10 mm or into reinforced concrete; pair it with tungsten-carbide SDS-Plus bits to DIN standards, and switch to diamond core drilling abov
Bridge-construction cut-off selection hinges on matching blade diameter, drive type, and abrasive bond to the member being cut — STIHL TS 420 class 14" gas saws suit rebar and formwork, while heavy-swing-frame 30" abrasive wheels like the Fox 2-C handle steel and casting sections on site.
Cut-off machines for tunnel construction split into three duty classes: 14-inch portable gas/electric hand saws (STIHL TS 420 class), 355 mm portable steel-cutting electric saws at 2200 W, and heavy swing-frame foundry cut-offs like the Fox 2-C with a 762 mm wheel at 30 HP. Match the class to ground

Landscaping cut-off work separates into two job families — green-wood pruning/limbing and hardscape masonry cutting — and the right machine is sized by blade diameter, no-load rpm, and rated wattage, not by brand. For limb work up to 115 mm, a 355 mm abrasive wheel at 4000 rpm and 2200 W covers the

HVAC cut-off machine selection hinges on matching the saw type to the duct, pipe, and rebar mix: 14 in. abrasive machines handle 115 mm round bar and 355 mm blade cuts, while gasoline TS-class units suit outdoor HVAC pad work.

Cut-off machines for electrical installation work are selected by blade diameter, motor power, and abrasive vs diamond wheel compatibility. The 110-125mm portable class runs 1400W at 220-240V; the 355mm stationary class runs 2200W at 3800-4000 rpm.

For masonry cut-off, dry diamond blades on a 14-16 inch portable saw or 20-26 inch walk-behind cover most block, brick and paver work; swing-frame abrasive machines apply only to foundry gate/riser removal, not masonry sizing.

Cut-off machines for demolition work split into three duty tiers: 1,400 W handheld 110/125 mm abrasive saws for rebar and small-section cutting, 30 HP swing-frame abrasive units at 14,200 SFPM for casting/riser removal, and 5 HP electrochemical NC stations holding ±0.01 mm on medical-grade tube. Mat

Cut-off machines for interior finishing fall into three duty classes — handheld electric (2200 W, 355 mm blade), swing-frame foundry (60–80 m/s wheel speed), and metallographic precision (≤203 mm wheel, X/Y/Z automated) — each matched to a different material and tolerance band. Selection hinges on s

For road maintenance cut-off work, specify 14-inch handheld gas cut-off saws for asphalt patch cutting, swing-frame electric units for rebar/dowel trimming, and match abrasive wheel speed (60-80 m/s) to the substrate. Pick by power source, blade diameter, depth-of-cut, and dust/water handling.

For steel construction, a 355 mm / 2200 W portable cut-off machine running ~3800–4000 r/min is the practical baseline for rebar, channel and pipe up to ~115 mm. Stationary TCT cut-offs (350–500 mm blade, 1100 r/min) suit fabrication-shop duty.
For bridge construction angle grinder selection, 125mm brushless cordless and 900-2200W corded 125-150mm models dominate 2026 OEM catalogues, matched to rebar, plate and concrete tasks with disc size, RPM and power as the three decision axes.

Angle grinders for tunnel construction are sized by disc diameter (110-180 mm typical industrial range), power class (2.5 kW pneumatic or 900-2200 W electric), and rotational speed (8,500-12,000 rpm), with selection driven by rebar cutting, concrete dressing and segment grinding duty rather than woo

For HVAC ductwork installation, a 4-1/2 in (115 mm) corded angle grinder with 1100–1300 W input, 11000–12000 rpm no-load speed, and a Type 27 (depressed-center) cutoff wheel sized 4-1/2 x 0.045 in is the working baseline, sized up to 7 in only for 12-gauge and thicker sheet-metal cuts.

For plumbing installation, select a 115 mm or 125 mm cordless brushless angle grinder with ≥9,000 rpm no-load speed, paddle or dead-man switch, and electronic anti-kickback; pipe-cutting is a secondary duty, not the primary use case.

For masonry work, pick a 100-125mm cordless brushless angle grinder (800-1000W class, 5500-7300 RPM) with a diamond cup wheel and dust shroud. Match the disc diameter to cut/grind depth and the motor power to stone hardness.
For demolition duty, an angle grinder typically requires a 180-230 mm wheel, 2000-2600 W input power, and a kickback-controlled soft-start; 115-125 mm units suit finishing only. Match disc to substrate: diamond cup for concrete, Type 27 depressed-center for rebar and steel.
For interior finishing, select a 100–125 mm cordless brushless angle grinder with variable speed (3000–11000 rpm), a paddle or dead-man switch, and dust-extraction readiness. Avoid large 180–230 mm masonry grinders, which are unsafe and oversized for finish work.

Road-maintenance angle grinders are typically 180-230 mm pneumatic or electric units delivering 2.0-2.5 kW at 6,500-12,000 rpm, sized to match abrasive diameter, dust environment, and surface material. Select by power source, wheel size, vibration, and dust-resistant construction rather than by bran

For concrete work, pick a 7-inch (180 mm) or 9-inch (230 mm) corded angle grinder rated 2,000 W+ with a dust shroud, matching diamond cup wheel, and sealed trigger. Small 115/125 mm cordless models lack the torque and disc size to grind cured concrete efficiently.
SDS-plus rotary hammers in the 2–4 Joule class cover roughly 90% of bridge deck drilling work; SDS-max and hydraulic breakers take over above 32 mm hole diameter or for demolition of formwork and bearing seats.

Landscaping crews should spec rotary hammers by chuck class (SDS-Plus vs SDS-Max), impact energy (2-12 J), and power source matched to the substrate: SDS-Plus cordless under 4 kg for stone wall chasing and fence-post anchors, SDS-Max 8 kg class for boulder splitting and concrete footing demolition.

HVAC duct and refrigerant-line work calls for an SDS-plus electric rotary hammer in the 5–7 kg class with 2–6 J impact energy, a pneumatic hammer mechanism, and triple-mode rotation stop; pneumatic 0.9–1.4 kg chipping hammers handle the lighter sheet-metal and bracket jobs per current DirectIndustry
Rotary hammer selection for electrical installation is driven by chuck type, impact energy, and ATEX class. For routine conduit and box fixing, an 800 W SDS-plus electric unit (2.8 kg, 24 mm concrete capacity) covers most tasks; pneumatic and hydraulic units are reserved for hazardous or wet zones.
Masonry drilling with rotary hammers is a chuck-class problem: SDS Plus 2-4 J for 6-13 mm anchors, SDS Max 8-19 J for 16-32 mm anchor and light chiselling, and pneumatic or hydraulic 6-80 bar above that for site utility, underwater, and ATEX work.
For interior finishing, specify a 1,200-1,600 W electric SDS-plus rotary hammer in the 5-6 kg class with 5-6 J impact energy, vibration-damped main handle, and selectable rotation stop; pneumatic scaling hammers in the 59-64 kg range are industrial surface-prep tools and the wrong category for finis

For road maintenance, choose SDS-Max rotary hammers in the 8 kg impact class with 12 J single-stroke energy and dual-mode (drill + chisel) function; pneumatic and 3-mode electric units also fit specific task profiles. Match chuck, power, and impact class to asphalt/concrete substrate rather than to

For steel construction, pick rotary hammers by chuck system, drive power source and impact class. SDS-Plus suits rebar and plate anchor work under 16 mm; SDS-Max 8 kg-class machines drive heavy demolition chisels over 12 J per stroke.

Rotary hammer selection for concrete hinges on chuck system (SDS-plus vs SDS-max), impact energy class (2-20 J), and weight tier (2-20 kg). Match 2-5 kg SDS-plus units to anchor and small-diameter work, 5-8 kg mid-class to general concrete drilling, and 8 kg+ SDS-max to heavy demolition.
Industrial hose reels divide into manual-rewind, self-retracting spring, and motor-driven classes, sized by hose I.D. (3/4"-1" typical), working pressure (20-350 bar), and length (10-83 m). Materials and seals are matched to media — stainless for washdown/chemical, polyester-coated steel for marine

Choose a hose reel by matching drive type, hose length/ID, working pressure, media compatibility and mount to duty. Self-retracting spring rewind suits 6-30 m air/water/oil service; manual for low-frequency shops; motorized for 35 m+ or workshop air-extraction. Verify NBR vs EPDM vs PVC inner tube a
Mezzanine platform suppliers cluster in Jiangsu and Shandong, China, offering rack-supported and structural-steel systems at US$0.80–80.00 with 1-ton or 1-piece MOQs; pricing is highly spec-driven, not list-driven. Global industrial buyers shortlist on load rating, floor decking, and standard compli

Mezzanine platform selection hinges on load class (125-1000 kg/m²), structure type, flooring, and code compliance (IBC, OSHA 1910.28). Match duty cycle, access method, and fire rating to the warehouse operation.
Storage rack system suppliers cluster in three regional hubs — China, India, and Southeast Asia — with 2,000+ vetted manufacturers on Made-in-China alone, FOB prices from US$0.70–1.00/kg for selective pallet rack and US$70–110/piece for steel storage cages, and lead times inside 15 workdays. For ASR

Selective pallet racks remain the default for most distribution centers, while push-back, drive-in, pallet-flow, mobile, and cantilever systems serve specific SKU-velocity, load-length, and density requirements. Medium-duty racks typically rate 200-500 kg per shelf level, and selective frames common

Picking an industrial workbench comes down to four spec gates: worktop material and thickness, load rating in kg, footprint in mm, and height adjustability. Match those four against the duty (light assembly, electronics repair, heavy fabrication) before comparing brands.

Hydraulic lift tables are sourced from a global pool of roughly 90 manufacturers offering 462 cataloged models, with China-led suppliers dominating entry-level 500-2000 kg scissor tables at US$79-US$5,000 FOB and European/US specialists covering heavy-duty dock and stainless sanitary builds.

Hydraulic lift tables split into three structural families — scissor (429 models listed), column-type (22) and bellows (10) — across 89 manufacturers tracked in mid-2026. Power source is the dominant decision axis: hydraulic 458 listings, electric 117, manual 86, electro-hydraulic 21 and pneumatic 2
Choosing a hydraulic lift table comes down to matching capacity, lift stroke, and drive type to the duty cycle. DirectIndustry's 2026-05-23 catalog lists 458 hydraulic models across 89 makers, with scissor dominant at 429 units, stationary at 314, and tilting variants around 32.
Resistance spot welding spans manual 48 kVA suspended guns, 600 kW–1.5 MW automatic mesh lines, and inverter or MFDC precision stations; selection hinges on weld thickness (0.5–6 mm steel), material (low-carbon steel, aluminum, coated sheet), and cycle/automation tier per current 2026 OEM catalogs.

Pick a spot welding machine by matching kVA rating, electrode force, current type (AC/ MFDC/inverter/medium-frequency), and cooling to your material stack-up. For thin steel/aluminum sheet, 14–31 kVA AC suspension units fit; for copper or micro-welds, inverter or 15 kHz medium-frequency models with
Laser welding machines deliver 10^4–10^7 W/cm² power density with non-contact keyhole fusion and several m/min travel speeds, while arc welders use lower-density electric-arc heating for thicker, heavier sections. Pick laser for thin-gauge, low-distortion, automation-friendly joints; pick arc for th

Laser welding machines split into four functional types — handheld fiber, CNC gantry, robot-integrated, and plastic/IR — and selection hinges on material, joint geometry, and power class (1,500–3,000 W dominant for metals).
Pick a laser welder by matching the laser source (fiber/YAG/CO2), power band (≈300 W spot, 1–6 kW handheld, 6 kW+ deep-penetration), and duty cycle to the workpiece's material, thickness, and reflectivity; verify cavity life, seam-tracking, and seam width capability before purchase.

Arc welding covers a family of processes — SMAW, GMAW/MIG, GTAW/TIG, SAW, PAW, stud/CD — each defined by electrode type, shielding scheme, and current polarity, with arc temperatures reaching 3500–4000 °C for general arc welding and roughly 6500 °F in tungsten-arc applications. Selection hinges on b

TIG welding machines split into DC-only, AC/DC, and inverter-class units; selection hinges on base metal (steel vs aluminum), thickness range, and duty cycle from 1.6 mm sheet to 6 mm electrodes.
China-based MIG welding machine manufacturers dominate global supply in 2026, with entry-level portable units priced from US$ 270-280/piece at 50-piece MOQ and industrial six-axis MIG welding robot arms quoted at US$ 9,000-70,000 per set on Made-in-China.com listings.

MIG welding machine types split along four decision axes: process mode (manual, semi-automatic, automatic, spot), inverter topology (conventional transformer vs IGBT), shielding gas (MAG/CO2/MIG-aluminum), and current class (single-phase 180-250A, three-phase 250-630A). The match between wire diamet
MIG welder selection hinges on matching duty cycle, output amperage, wire-feed platform and input power to the workpiece thickness and duty mix. Industrial-grade IGBT inverter units typically deliver 200-350 A at 60% duty cycle, while home/hobby models cluster at 140-200 A with lighter duty.

Cast aluminum alloys and aluminum ladders share a base metal but diverge sharply in alloy system, forming process, mechanical targets, and procurement specs. Pick cast aluminum when you need complex 3D geometry plus 240-360 MPa tensile strength; pick aluminum ladder extrusions when you need 6061/606
Aluminum coil and aluminum ladder are not competing products — they sit at different points in the same extrusion-and-rolling supply chain. Choose by form factor: coil for downstream stamping/forming of roofing, cans, and cladding; ladder for finished access equipment built from extruded profiles.

Aluminum sheet and aluminum ladder share the same base metal but diverge sharply on form, alloy selection, and tolerance. Sheet stock (0.15-200 mm gauge, up to 16 m length) is the feedstock for downstream fabrication, while ladders are finished extruded products rated to 3.6-7.5 m working height and
Aluminum extrusion profiles (primarily 6063-T5/T6 and 6061 alloys, anodized or powder-coated) and aluminum ladders (made from the same 6000-series extrusion feedstock) share a common billet-to-billet production path but diverge on cross-section complexity, MOQ economics, and end-use certification. 2

Mobile scaffold towers span three material families — aluminium rolling towers, hot-dip galvanised steel Ringlock, and GRP/fiberglass — with current export FOB price bands from Made-in-China listings at US$700-1,800/set for aluminium and 20-day lead times. European OEMs (Altrex, Hünnebeck, ZARGES, W
Frame scaffolding vs modular (system) scaffolding: choose frame for low-rise facades, brickwork, and short-cycle plaster/paint jobs under 30 m; choose system (ringlock/cuplock) for irregular facades, industrial plants, and shoring above 30 m. Steel grade Q235, 42 mm main tube × 2.2 mm wall is the do
Frame scaffolding from Chinese manufacturers is widely available in Q3 2026 at US$ 5-750/Ton across H-frame, door-frame, walk-through and step-frame variants, with EN 12811 compliance common and MOQs from 1 Piece to 10000 kg.

Frame scaffolding divides into A-frame (door/trestle), H-frame (ladder/mason/walk-thru), arch, and rolling-tower variants, with steel 1.69" OD tube dominant in US/EU markets and aluminium used for mobile towers. Selection hinges on bay width, load class, and whether the work face is interior masonry

Cuplock scaffolding is a modular steel system built around top-cup/bottom-cup node connections on 48.3 mm OD verticals, with standards spaced at 500 mm cup intervals. Eight structural categories — standards, ledgers, transoms, diagonal braces, planks, base jacks, cantilever/side brackets, and top-ac

Ringlock scaffolding is a modular, multidirectional system built around a 133 mm rosette and wedge-head connection on Q235/Q345B verticals (typically D48×3.5 mm), with 80% of components reusable across applications; it suits high-load, irregular-geometry sites but trades off against cuplock, frame,
Ringlock scaffolding supply is concentrated in Chinese manufacturers offering hot-dip galvanized Q235/Q345 steel standards, modular wedge connectors, and MOQs from 1 m² to 20 m.t. with monthly capacity up to 10 million m². Buyers should match supplier by steel grade, tube size (typically D48.3 mm),
Ringlock scaffolding is a modular rosette-node system built around vertical standards with fixed Ø48 mm or Ø60 mm discs, horizontals, and ledgers priced roughly US$3.00-20.00 per piece. Selection hinges on ledger outer diameter, hot-dip galvanizing, and duty classification rather than brand alone.

Vibrating fork level switches suit liquid point detection at low cost and IP67 hygienic builds; laser level sensors win on non-contact, millimeter accuracy for bulk solids and harsh surfaces. Pick by media, accuracy, and mounting.
Capacitance level sensors and laser level sensors solve different jobs: capacitance handles conductive liquids, interfaces and harsh chemicals (DC>1 μS/cm needed), while laser measures bulk solids and opaque liquids up to 48.77 m contact-free. Pick by medium dielectric, distance, viscosity and conta

Ultrasonic level sensors suit liquids, sludge, and bulk solids in storage tanks at ranges up to 15 m, while laser level sensors target short-range, high-precision positioning. Pick by medium, range, and beam behaviour, not brand.

Guided wave radar (GWR) and laser level sensors occupy different niches: GWR handles bulk liquids, interfaces and solids up to 75 m at 400 bar / 450 °C, while laser levels target short-range, non-contact positioning. GWR suits harsh, dirty or foam-laden process tanks; laser suits precision positioni

Non-contact radar level transmitters dominate process storage and bulk-solids measurement with 30-40 m range and 200 °C process limits, while laser level transmitters target short-range, high-precision tasks in a market valued at $136.34 M (2025). Choose radar for tanks, silos, corrosive media and s
A concrete pump truck and a concrete vibrator solve two different jobs on the same pour: the pump moves 30–170 m³/h of fresh concrete vertically and horizontally, while the vibrator consolidates already-placed concrete at 3,000–12,000 vpm. For slabs, walls, and columns under 8 m, the vibrator is the
Concrete batching plants and concrete vibrators solve different problems on the same job site: batching plants dose, weigh and mix structural concrete at 45-180 m³/h output bands, while vibrators consolidate fresh concrete in-place via high-frequency insertion or external form-mount action. Pair the

Concrete mixer trucks and concrete vibrators solve different problems on a pour day: trucks transport and agitate 6–12 m³ batches while rotating 2–6 rpm, vibrators consolidate already-placed concrete at 3,000–12,000 vpm. Choosing the wrong primary tool costs either slump loss during haul or honeycom

Core drilling machines cut clean circular holes in masonry, concrete and rock using an annular bit; impact drills drive a twist bit with rotary + percussive force. Pick the core drill for diameters above ~12 mm in mineral substrates, the impact drill for small-diameter fasteners in wood, metal, and

A rotary drilling rig is a 25-tonne-class crawler or truck-mounted machine (e.g., RTD45 at 403 kW / 30.97 m depth) engineered for 95-165 mm blasthole and geotechnical work, while an impact drill is a 1-1.5 kW handheld power tool using 6-26 mm bits for concrete or masonry. Match the machine to the ho

Oxy-fuel cutting torch TCO over a 10-year horizon is dominated by consumable gases (acetylene/propane/oxygen), nozzle/tip replacement, and CNC table utilisation, not by machine purchase price. Driver ranking: fuel-gas mix > electrodes/nozzles > power > maintenance labour > depreciation.

Oxy-fuel cutting torch: thick-plate workhorse from 0.5 mm to 300 mm, low capex, oxidising-only — cannot cut stainless, aluminium, copper, or any painted/rusty mild steel. Pick it for heavy carbon steel and structural plate; pick plasma for everything else.

Oxy-fuel cutting torch installation follows a four-gate path: torch + nozzle selection, gas train assembly, height/ignition setup, and commissioning checks. Manual torches such as MESSER SMB 663 cut up to 700 mm; integrated magnetic height sensing in the ALFA removes external sensing rings.
Oxy-fuel cutting torches split into three classifications by duty: hand/semi-automatic torches for field work, machine torches for CNC gantries, and heavy-duty torches for steel-mills. Fuel-gas selection (acetylene, propane, MAPP, propylene, natural gas) and torch type together define cut quality, t

A plasma cutter's true 5-year cost is typically 2.2-3.5x its purchase price once consumables, power, compressed air, and downtime are counted. The biggest cost drivers are electrode/nozzle sets and electricity, not the machine itself.
Plasma cutter installation is a four-gate job — input power, compressed-air supply, torch/consumable stack, and grounding/work-clamp — and missing any one gate causes blown contactors, poor cut quality, or torch failure. Hypertherm Powermax30 AIR delivers 15–30 A with 8–16 mm severance on a 240 V si

Plasma cutters are classified by operating mode (manual/CNC/automatic), power-source topology (inverter-dominant), pilot-arc method, and process gas (air, O2, N2, Ar-H2). Selection gates on max current, severance thickness, duty cycle, and material; CNC HF-start systems can interfere with nearby dig

TIG (GTAW) delivers the cleanest, most controllable fusion weld for stainless, aluminum, and thin-gauge work, but pays for it in slower deposition, stricter operator skill, and higher equipment cost than MIG or stick.

TIG welding machine installation is a 4-step site workflow: mains verification (230V single-phase or 400V three-phase per nameplate), VRD and fuse check, gas/coolant circuit purging, then parameter set-up via EASY or PRO mode. Skip any step and you risk warranty voiding, electric shock in damp envir

TIG welding machines are classified by current mode (DC, AC/DC, pulse), automation (manual, semi-automatic, fully automatic), and process variant (seam, orbital, inverter). Selection pivots on base metal, thickness, weld profile, and production volume rather than brand.

Arc welding machine total cost of ownership is driven by inverter class, duty cycle, electrode/wire consumables, energy, and shielding gas; IGBT inverter MMA units from Wuxi Hanshen and Indian OEM lines tracked on 2026-07-22 show the purchase line is only 25-40% of five-year TCO, with power, electro

Arc welding machines join metals with an electric arc and remain the lowest-cost, most portable joining method for steel work, but productivity, distortion, and operator-skill demands vary sharply by process variant such as SMAW, GTAW, and plasma.
Arc welding machine installation hinges on matching the power source to input supply, dedicating proper cable cross-section, grounding the work clamp to clean bare metal, and verifying the inverter's duty cycle. Skip the ground clamp, undersize the leads, or run on an unvented circuit and you get vo

Arc welding machines span six core process families — DC/AC metallic arc, carbon arc, atomic hydrogen, shielded metal arc (SMAW), MIG/MAG, and TIG — differentiated by electrode type, current polarity, shielding gas, and arc temperature of roughly 3,500–4,000 °C. Selection hinges on base metal, thick

An aluminum ladder's true cost over a 10-year fleet lifecycle is dominated by replacement frequency, worksite damage, and alloy-grade selection, not the sticker price. Spec-driven TCO modeling separates a $180 unit that costs $900 from a $260 unit that costs $620.

Aluminum ladders typically weigh 30–50% less than equivalent steel ladders and resist corrosion without painting, but they cost more per rung and conduct electricity. The right pick depends on workload, environment, and electrical exposure, not just weight.

A suspended working platform is a temporary, suspended access system that hangs from roof-mounted rigging to carry workers, tools and materials at building facades, bridges and high-bay industrial structures. Compared to mast-climbing work platforms and tube-and-coupler scaffolding, it delivers fast

Suspended working platform (ZLP series) installation hinges on roof rigging, wire-rope hoist verification, and safety-device interlocks before first ascent. Capacity bands 250-630 kg, modular lengths to 15 m, lifting speeds near 9.6 m/min dominate 2026 build specs.

Climbing formwork total cost of ownership runs 3-5x the bare purchase price once crane time, labour, climbing-cycle cycle-time losses, and re-use spreads are loaded. Drivers ranked: cycle time per lift (hours), re-use count over the structure, crane dependency vs self-climbing, and on-site labour ho

Climbing formwork delivers crane-independent, hydraulically powered vertical cycling for cores, shear walls, and high-rise shafts, but trades that speed for higher capex and strict structural-prep requirements. The decision hinges on pour-height cycle, geometry regularity, and crane access.
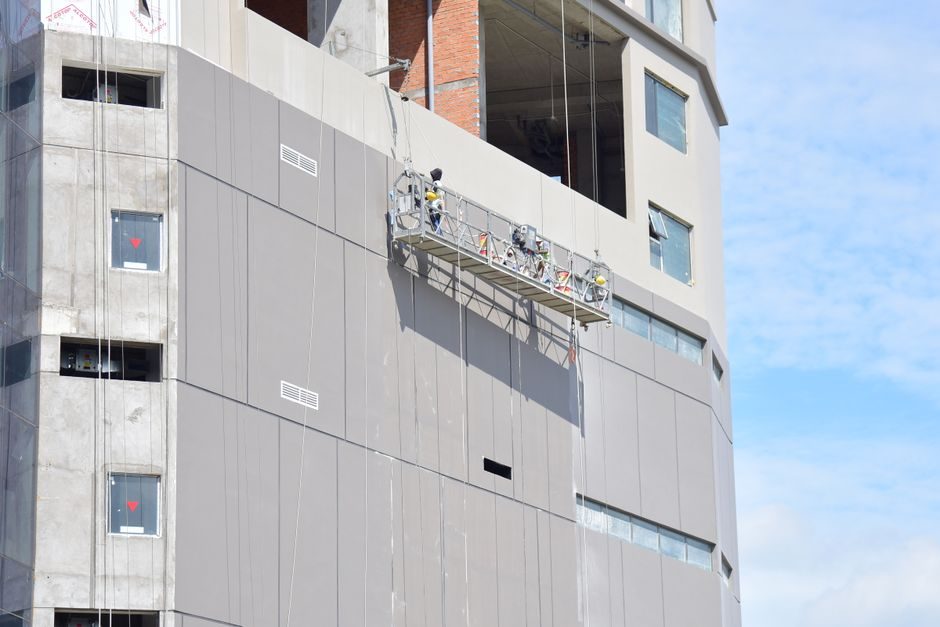
Climbing formwork systems lift a working platform upward to pour vertical concrete lifts in skyscrapers, bridge pylons, and dams. Auto-climbing units built on 6061-T6 aluminum or Q235 steel self-reposition on rails between pours, cutting crane time and labor on tall structures.

Climbing formwork splits into three principal families — manual crane-lifted, hydraulic self-climbing (ACS), and rail-guided automatic — with 6061-T6 aluminium and hot-dip galvanised steel as the two dominant structural materials, and core-wall / high-rise applications specifying each type by cycle-

Scaffolding TCO is dominated by labour, not purchase price: typical lifecycle spend splits 60-80% to erection/dismantling labour and 20-40% to materials, with safety incidents and re-erection cycles driving the largest variance between contractors.

Tube-and-clamp scaffolding delivers the lowest per-meter cost and highest site flexibility, but its labour and safety overhead push contractors toward modular systems on tall or repetitive builds. Hot-dip galvanized diagonal braces at 2.5 mm wall thickness remain the baseline corrosion-protected spe

Field-installed scaffolding on commercial and industrial sites follows British Standard BS 5975 / EN 12811 conventions, with the height-to-base-width 3:1 tie-off rule and ISO 9001-erected quality systems as the recurring baseline. Use this guide to choose independent, tower, platform, or hanging sys

Infrared line level TCO is dominated by 5-10 year service-life variables, not the sensor head's purchase price. Acquisition typically represents 20-35% of lifetime cost, while calibration, optics cleaning, installation labor, and downtime drive the remaining 65-80% across industrial deployments.
Infrared line levels project a non-visible 635-905 nm laser line for single-person layout over 3-30 m, costing 60-85% less than rotating green-beam systems. Trade-offs: limited visibility under 500 lux ambient, fixed line geometry, and 2-4 mm accuracy drift beyond 15 m on uneven floors.

An infrared line level projects a 180° or 360° plane from a single laser diode — red (635 nm) or green (532 nm) — and is classified under FDA/IEC laser power tiers, with most leveling tools landing in Class IIIA (1–5 mW) and accuracy spanning ±1/8" to ±1/2" at 50 ft.
Laser distance meter total cost of ownership is dominated by purchase price, battery cost, calibration drift, and repair exposure, with ISO 16331-1 certified models cutting re-measurement rework on site. Across 30-120 m class units, entry modules run $90-150 while feature-loaded instruments reach $1

Laser distance meters deliver ±1.5 mm to ±20 mm accuracy over 40 m to 2,500 m ranges, but fail on transparent, dark, or angled surfaces without a target plate and cost more than 5 m tape measures. Time-of-flight industrial units like the RIEGL LD05e-A suit harsh outdoor surveying, while pocket 40-12

Laser distance meter installation in industrial settings is a three-stage process: target-and-reflector geometry, mounting/alignment, and interface commissioning. Field-engineered units such as the TR-Electronic LE25 reach 25 m with 0.1 mm precision; handheld tools like the Fluke 417D work to 4

Laser distance meters split into portable handheld units (0.05-100 m, phase-shift) and fixed long-range time-of-flight sensors reaching 2,500 m, with selection driven by range, accuracy, and laser class. Pick handheld for interior layout, fixed ToF for surveying and rail clearance. RIEGL LD05e-A30 a
Theodolite total cost of ownership over a 10-year service life is driven less by instrument purchase than by calibration labor, battery logistics, crew-day rates, and accessory replacement. A spec-driven TCO stack runs $45k–$180k per unit depending on angular accuracy class and field-deployment inte
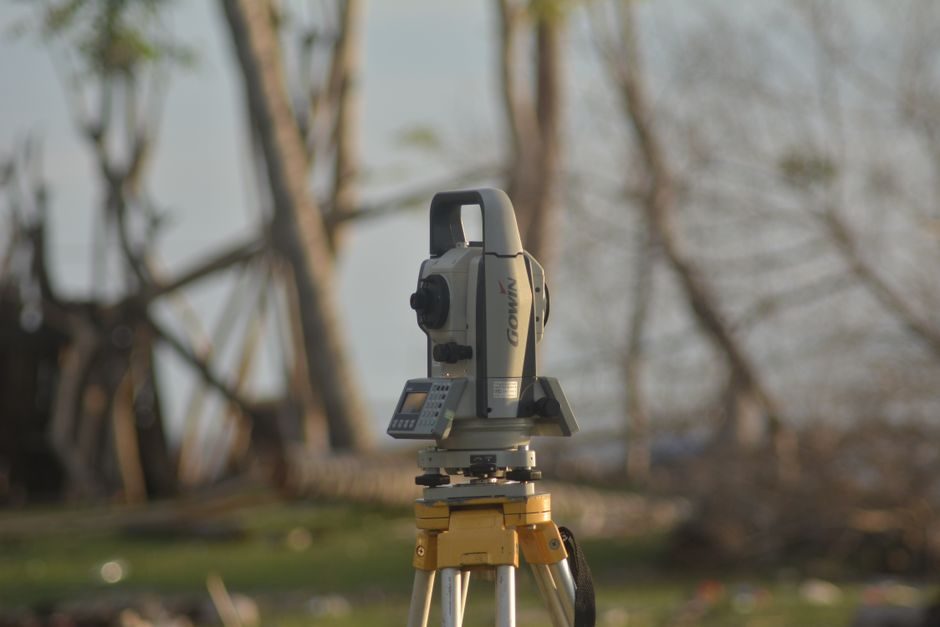
Theodolites deliver sub-second angular accuracy over kilometer-scale baselines but trade that off against cost, training overhead, and line-of-sight dependency versus total stations, GNSS, and laser scanners. Choose a theodolite when sub-arc-second mechanical reliability matters more than digital da

Automatic level total cost of ownership spans a 10-15 year service window, where purchase price is typically 20-30% of lifecycle cost; energy, calibration, and sensor replacement dominate the rest. Buyers should run a TCO model that weights MTBF, laser drift, and field-service hours before selecting

Total station total cost of ownership over a 10-year service life typically runs 1.8x to 2.5x the acquisition price, dominated by calibration, operator training, EDM prism consumables, and firmware-renewal fees. Spec-driven buyers who lock accuracy class, IP rating, and service contract terms at RFQ
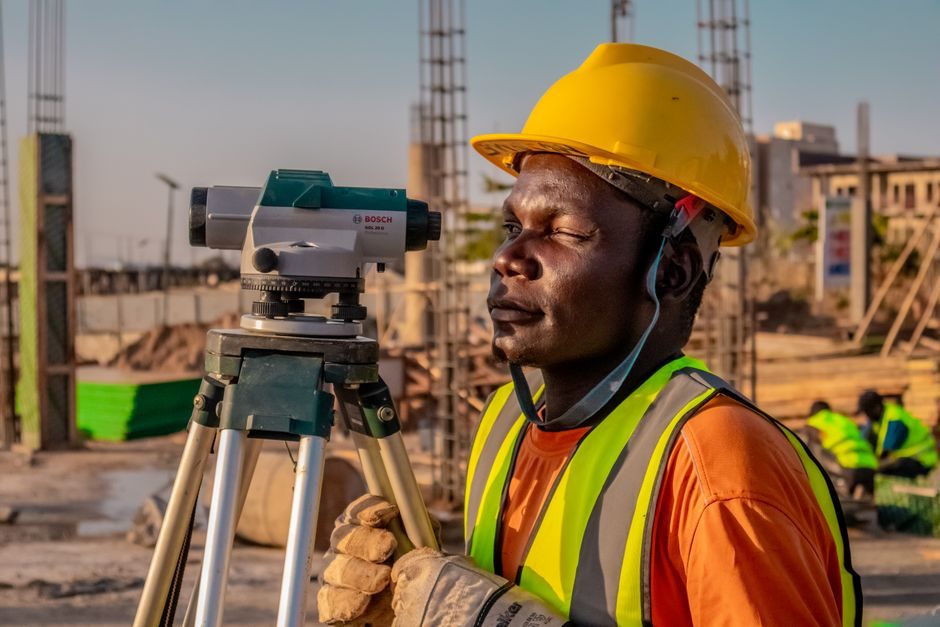
A total station combines an electronic theodolite with an Electronic Distance Measurement (EDM) module, delivering angle and distance data in one instrument with sub-second angular accuracy and millimeter-class distance precision, which makes it the default tool for surveying, construction layout, a
Total stations are classified by accuracy, range, automation and servo control — from 2" manual units to 1" robotic models with 6000 m prism range and IP65 housings. Selection is driven by order of survey (second/third/general), angular accuracy, and reflectorless distance capability.
Laser level total cost of ownership runs 2.5x to 4x the unit sticker over a 10-year service life. Acquisition, calibration cycles, battery wear, diode degradation, and operator rework drive the gap.
Laser levels project a self-levelling reference beam across a worksite, trading the time-cost of a spirit level for line-of-sight, ambient-light, and battery limits. Choose green-beam 360° units indoors; choose pulse-receiver-capable red-beam or rotary units for outdoor runs over 30 m.

A correctly installed laser level combines a calibrated self-levelling instrument, a rigid tripod or wall mount, and a matched detector or target, with rotary, line, and point classes requiring different setup tolerances and power arrangements on indoor and outdoor sites.

Laser level types split into four working classes — rotary, cross/multi-line, line/spot, and point/plumb — selected by beam geometry, range, accuracy, and detector pairing. UK spec catalogues published 2026-07 list Topcon RL-H5A, Leica, Fukuda, and Spectra Precision rotary kits alongside Spot-On gre
Shotcrete machines deliver high-output, pneumatically projected concrete for tunnels, mines, pools, and refractory work, but rebound loss, dust, and compressed-air demand drive their main disadvantages. Selection hinges on wet vs dry process, output rate, and accelerator compatibility.
Wet-mix and robotic shotcrete machine installation demands matched power, water, and air rigging before hose string-up, with a documented 0.5-1.0 MPa trial shot and 75-100 mm slump check. Crews skipping these steps typically see rebound above 25% and boom-pressure alarms within the first hour.

Shotcrete machines split into dry-mix and wet-mix families, then into portable, truck-mounted, and robotic classes, with output ranging roughly 4-30 m³/h and pumping pressure up to ~70 bar. Selection hinges on mix-water control, dust exposure, reach, and tunnel/open-pit duty. Robotic wet-shotcrete u

Floor grinder TCO spans acquisition (35–55%), consumables (15–25%), power and dust extraction (10–20%), and maintenance/disposal (10–20%), with planetary vs. rotary head class driving the largest cost split. Choosing 380V three-phase over 220V single-phase typically halves the 5-year energy line.
Floor grinders deliver 5-10x faster concrete surface preparation versus hand grinding but require dust extraction, trained operators, and careful substrate matching to avoid damage. The right machine cuts cost; the wrong one burns labor and re-work.
Floor grinder installation is a substrate-prep workflow, not a tool-mounting job: success depends on flatness tolerance, dust extraction CFM, and matching head/abrasive to concrete hardness. Walk-behind planetary and edger classes dominate the 2026 rental and contractor fleet, with single-disc units
Floor grinders split into three structural families — single-disc, multi-disc/planetary, and ride-on planetary — distinguished by power source (110-220V single-phase, 380-415V three-phase, or thermal), working width (250 mm to 2,150 mm), and weight class (45 kg to 3,035 kg). Selection hinges on job
A concrete groove cutter delivers a narrow, controlled cut in cured concrete or asphalt at depths of roughly 5–75 mm with a diamond or abrasive blade, but the trade-off is heavy machinery, dust and slurry, and hard limits on steel-reinforced slabs.
Concrete groove cutter installation hinges on matching blade diameter (700-900 mm) and motor power (up to 45 kW) to slab thickness up to 300 mm, with a 1,000 L water tank, e-stops and blade-lid guards mandatory on semi-autonomous rigs like the Prensoland CR-900.

Concrete groove cutters split into manual, walk-behind, hand-held, self-propelled floor saws, wall-mounted track saws, and wire saws, with power from 3 kW hand tools to 75 kW diesel road units. Selection hinges on cut depth, blade diameter, power source, and dust suppression.

Laser screed TCO spans a 7-10 year service window where acquisition covers 45-55% of lifetime cost, while maintenance, downtime, and energy move the rest. Cost drivers: machine class, power source, automation grade, and floor-area volume. Total cost over 100,000 m² typically runs 1.6-2.4× the purcha

Laser screeds deliver flatness of FF 50/FL 40 or better on 5,000-10,000 m²/day pours with a 4-6 person crew, but require 150-300 kVA generators, 10-15 cm minimum slab depth, and cap on column spacing that rules out warehouse retrofits under 3,000 m².
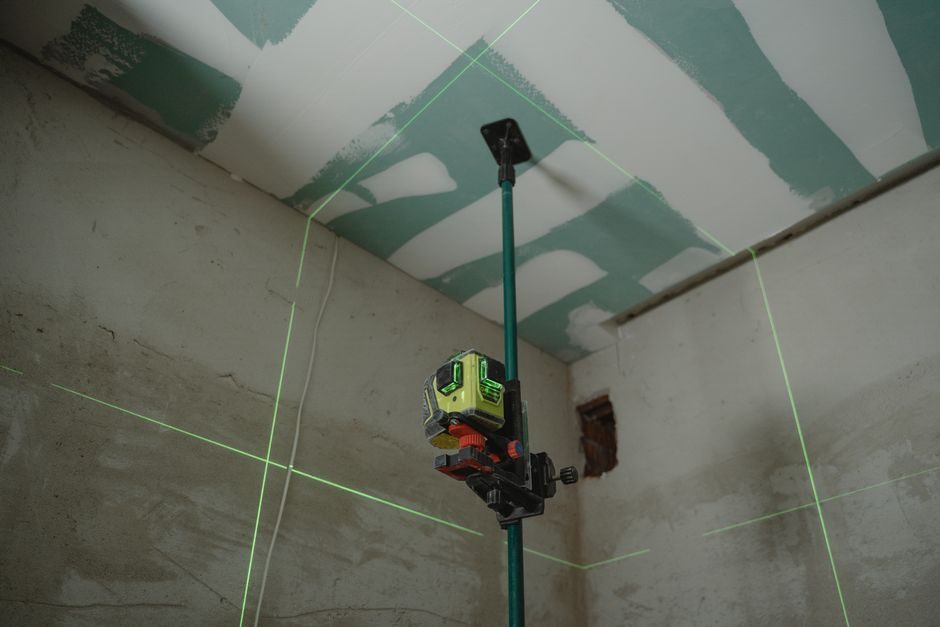
A laser screed installs a flat floor concrete slab by combining a rotating laser reference plane with a hydraulic plow head and auger strike-off, hitting Ff/Fl 30-50+ on a single pour. The installation guide covers sub-base prep, machine selection, and pass sequencing for slabs from 5,000 to 100,000
Laser screeds are classified by drive type (walk-behind, ride-on, boom), head type (auger, plow, roller, 3D profiler), and power source, with selection driven by slab size, FF/FL tolerance, and pour volume. Walk-behind units cover small pours under ~200 m²; ride-on and boom machines dominate commerc

Walk-behind and ride-on power trowels deliver 10× the concrete finishing productivity of hand-floating, but only when matched to slab size, blade type, and operator skill. Below: the working envelope, the failure modes, and the cross-criteria scorecard.

Power trowels are classified by power source (gasoline, diesel, electric, battery), operator configuration (walk-behind vs ride-on), and blade geometry (float pan, finish, combination), with rotor diameter and engine power band determining slab size fit.
Immersion-type concrete vibrators are specified on roughly 90% of cast-in-place pours over 1 m thick, but on thin slabs and dense rebar cages the form-attached (external) type often outperforms them. Choose by element geometry, rebar density and slump, not by headline price.
Electroslag pressure welding (ESW) delivers single-pass joins on 25-300 mm vertical plate at up to 20 kg/h deposit rate, but coarse grain and high HAZ hardness restrict it to thick low-carbon steel.

Rebar coupler TCO hinges on five drivers: purchase unit price, certified installation labor, lap-length rebar savings, inspection/replacement cycles, and project-stage volume tier. A spec engineer who runs the full life-cycle math, not the per-piece sticker, can shift 5-year spend on a 10,000-couple
Field-install a rebar coupler in four controlled steps: cold-cut the bar end square, upset or roll-parallel the threads, torque the sleeve to the maker's value, then proof-test to ISO 15835 / AC-133 slip and fatigue limits before pour.

Rebar couplers are mechanical splices classified by load-transfer mechanism — upset-forged parallel thread, cold-extrusion, grout-filled, wedge-lock, weldable, and end-anchor types — typically covering Ø12–40 mm bar (ASTM #4–#8) with tensile strength ≥800 MPa, designed to meet ISO 9001, ACI 318, BS

A rebar threading machine TCO model must capture six cost lines — machine, dies, energy, labor, downtime, and rebar waste — because the purchase ticket is typically only 30–45% of 5-year spend on rebar processing lines.

Rebar threading machines deliver faster, higher-strength mechanical splices on bars from 12 mm to 50 mm versus lap welding, but they carry a higher per-bar capex, demand tight thread-tolerance QC, and add on-site power and consumable cost. Use them on high-volume, high-bar-count pours; skip them for

A rebar threading machine installs correctly when bar-end prep, machine sizing, and torque-controlled coupler makeup are each matched to rebar grade and diameter. Use 40CR/45# carbon-steel couplers, validate threads with plug/ring gauges, and tighten with a calibrated wrench.
A rebar straightener pulls coiled or bent bar back to within ≤2 mm/m straightness tolerance at 30–80 m/min, replacing slow manual chisel work. Trade-offs: 1.5–8 kW motor draw, die wear on rebar above 500 MPa yield, and 3–6 m² floor footprint per machine.

A rebar straightener installation follows a clear six-step sequence: site prep, anchoring, leveling, power wiring, lubrication, and trial run. Selecting the right model (YG-6 to YG-16, 5.5-15 kW, 4-12 mm capacity) is the first decision, since most field failures trace back to undersized motors or sk

Rebar cutter 5-year TCO is dominated by blade set replacement, electrical energy, and operator labour — purchase price is typically 15-25% of lifecycle spend. Hydraulic and electric models diverge sharply on energy cost and blade-change downtime above 2,000 cuts per week.

Rebar cutters deliver clean, code-compliant shear cuts on site, but their power source, blade class and bar-diameter ceiling decide whether they fit a project. This 2026 spec reference maps hydraulic, electric and manual cutter trade-offs against rebar grade, diameter and daily cut count.

Electric rebar cutters sized 10–42 mm require matched blade sets, dedicated 3-phase supply, and torque-checked mounting before first cut. This 2026 field reference walks site prep, mechanical mounting, electrical hookup, blade change, and acceptance-test procedures, with model-specific blade part nu
Portable hydraulic rebar cutters dominate job-site use up to 1" (#8) grade 60, while industrial shear lines and rotary/bender-cutter combos cover higher-capacity fab and continuous production. Selection pivots on bar diameter, cycle rate, power source and blade geometry, not on brand alone.

Rebar bender TCO hinges on five drivers — machine class, mandrel/bending pin set wear, electric kWh per tonne bent, die change labour, and service contract scope. A benchtop GW40 unit lands 65-75% below an industrial CNC GW50 over 5 years when annual throughput stays under 800 tonnes.

A rebar bender replaces manual bar-bending labor and lifts hourly output from roughly 50 pieces to 600-1200 pieces per shift on #4-#6 rebar, but it brings 380-440V three-phase power demand, 1.5-3 t stationary mass, and recurring collet/mandrel wear that drive operating cost. Spec the machine to bar

Portable hydraulic rebar benders in the 180 lb class bend 1" (#8) grade 60 rebar on 110 V site power, and acceptance hinges on footing, power, and bending-angle calibration. Wrong pickup weight or undersized rebar class voids the bend and risks pin shear.

Rebar benders fall into five working classes — manual, electric, hydraulic, CNC and portable — selected by bar diameter, bend volume and site power. Capacities run from light #5 (16 mm) portable units up to #14 bar (≈45 mm) hydraulic shop machines, with angle range typically 0–180° and compliance to
Air pick total cost of ownership typically breaks down into five lines: tooling, air-prep energy, consumable wear parts, labour and downtime. Over a 5-year service life purchase price averages 30-40 percent of TCO, while compressed-air energy and downtime drive 45-55 percent. The single largest cont

Air picks (pneumatic picks) deliver high striking energy with no spark risk, but trade off on noise, vibration, consumable wear and air-system overhead. Use them for chipping concrete, descaling boiler tubes and demolition in flammable atmospheres; avoid them for fine finishing or remote-cab work.

An air pick is a pneumatically driven hand tool that accelerates compressed air through a converging/diverging nozzle to supersonic velocity and uses the resulting jet to fracture, pulverize or displace target material without cutting it. Three operating parameters define its class: inlet air volume

An air impact wrench's 5-10 year total cost is driven by air consumption, hammer-mechanism wear, and consumables — the tool body is often under 20% of lifetime spend. Fleet TCO math favors mid-tier guns at 6.2-7.0 CFM over the cheapest bid.

An air impact wrench delivers the highest torque-to-weight ratio of any handheld fastening tool, but trades that power for a hard airline, an FRL, and a controlled duty cycle. Choose it for assembly-line and wheel-service bolting; skip it for field service far from a compressor or for low-cycle prec

Air impact wrenches are installed by matching drive size, air-supply class, and torque output to the fastener, then commissioning a 90 psi (6.2 bar) clean dry airline with the correct hose and lubricator. Shop 2026 listings of 1/2", 3/4" and 1" drive pneumatic impact wrenches confirm the procedure a

Pneumatic nail gun TCO over a 3-5 year window runs roughly 25-40% tool purchase, 30-40% compressor energy, 15-20% consumables and 10-20% maintenance, dominated by air supply and jam downtime. Tool-only purchase hides most of the real spend.

Pneumatic nail gun installation hinges on matching compressor supply (typically 5-7 bar), air-inlet fitting (1/4" NPT standard) and nail-length range to the framing vs finishing duty cycle before any trigger is pulled.

Stud welder installation hinges on matching the process (CD, Short Cycle, Drawn Arc) to base metal, stud diameter, and available amps; primary power 3-phase 400-480 V or single-phase 230 V, dedicated circuit, ≤4 m gun lead, and a clean, oil-free weld zone are the hard gates before striking an arc.

Three principal stud welding processes — Capacitor Discharge (CD), Drawn Arc (DA), and Short Cycle (SC) — cover diameters from roughly 3 mm to 25 mm and parent materials from sheet steel and stainless to aluminium and brass, making stud welding one of the strongest single-side fastening methods used

A sander is a portable surface-finishing power tool that drives an abrasive sheet, disc, belt or pad against a workpiece to remove stock, smooth welds, or prepare coatings. Selection hinges on abrasive format, orbit diameter, dust extraction, and duty class — there is no single best type.

Floor sander installation centers on drum sander, edger sander, and buffer setup with proper paper-attach (hook-and-loop), grit sequencing, dust-bag fitting, and dust-port vacuum hookup per OEM PDF guidance.
Power mixer TCO runs 2.2× to 3.5× the purchase price over a 10-year life when energy, wear parts, downtime and disposal are included, with the motor-drive and seal-replacement lines dominating 60-70% of lifecycle spend.

Power mixers deliver high-shear, high-torque mixing for slurries, concrete and resins but carry motor-oversize, seal-wear and dust-explosion trade-offs. Selection hinges on viscosity band, ATEX/IECEx zone and IP rating.

Demolition hammer TCO over a 5-7 year service life is dominated by energy, chisel/bit wear and downtime, not by the €150-€900 purchase price. A concrete TCO line-by-line model for corded 1500-2000 W, cordless 18-54 V, and pneumatic classes is laid out here with selection rules and a verifiable per-h
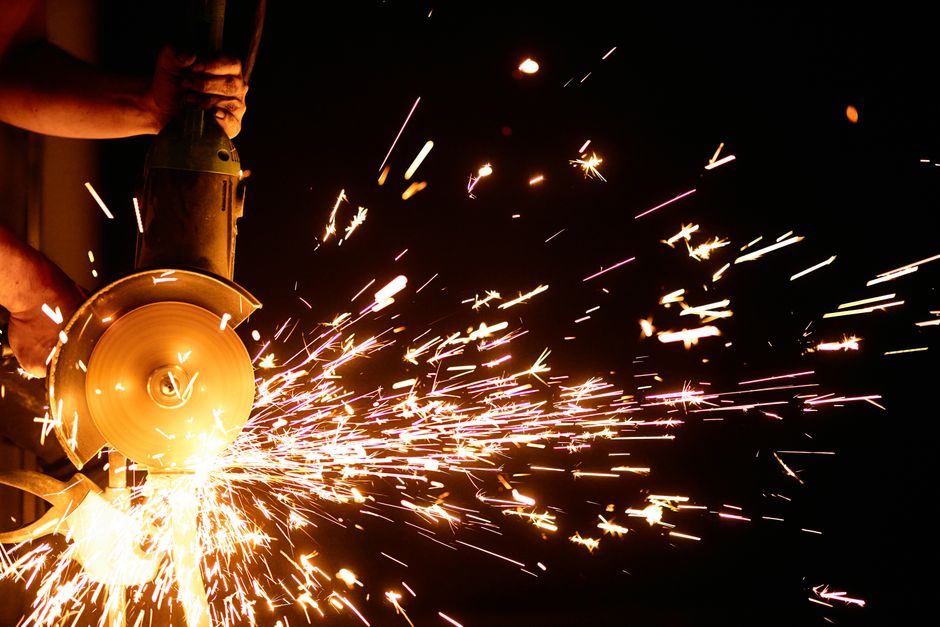
For a 7-inch marble cutter running two shifts on a tile-fabrication line, the purchase price covers only 10–30% of the 5-year lifecycle cost; blades, diamond-segment wear, downtime, water/coolant, dust-extraction energy and operator PPE dominate the TCO ledger and the decision matrix.
Marble cutters deliver narrow-kerf, vibration-controlled stone cutting with 110–125 mm diamond blades and 30 mm depth per pass, but trade off portability, dust load and electrical risk. Choose wet-feed models for indoor marble; pick angle grinders instead for general masonry.
Field installation of a circular saw hinges on blade-guard integrity, guide-rail flatness to within 0.1 mm, anchoring to a 315 mm-class reinforced table, dust extraction routing, and 0° calibration before the first cut. Skipping any of these gates turns a precision tool into a kickback hazard.

A circular saw is a power saw with a toothed steel disc rotating on a spindle, classified by power source, frame type, blade material and material-to-cut. Common types include handheld, miter, table, cold cut, carbide-tipped, diamond and HSS variants.

TCO for an impact drill is dominated by energy, consumables, downtime and service over a 3–5 year window — sticker price is typically under 30% of total spend. Industrial corded 800–1500 W models run 50–200 Wh per shift, while pneumatic units shift cost to compressor air at 100–600 L/min per tool.

Impact drills deliver 0–3,000 BPM hammer action and 60–80 N·m max torque in a single pistol-grip tool, but add 0.7–1.5 kg over a standard drill and cost 2×–3× more for the same chuck size.
Pneumatic impact drill ST-4250 specs: 1,000 RPM free speed, 16 mm (5/8") drilling capacity, 420 mm length, 3/8" PT inlet, 708 L/min (25 cfm) air consumption, 6.3 kg net weight. Use this guide to set air supply, side-exhaust ducting, lubrication, and safe-handling steps before each shift.

A cut-off machine is a stationary or portable abrasive saw that uses thin reinforced resin-bonded wheels (typically 1.0–1.6 mm thick) to sever metal, stone or alloy stock; trade-offs center on kerf loss, heat input, wheel cost and dust control.

Portable 355 mm cut-off saws at 3800 rpm and 2200 W remain the dominant shop-floor abrasive cutoff configuration per mid-2026 manufacturer listings, with installation gated by blade guarding, wheel-speed matching and supply-voltage selection.

Angle grinder TCO spans acquisition, consumables, energy, downtime and PPE; wheel cost and downtime dominate over 5 years, and 1,200 W brushless platforms cut energy roughly 20-30% vs older universal motors.

Angle grinders in 4½" to 9" disc sizes cover cutting, grinding, sanding and rust/paint removal across metal, masonry and concrete, with disc RPM and motor amps as the two primary selection gates.
Angle grinders are classified by disc diameter (100/115/125/150/180/230mm), power source (corded vs cordless), and spindle thread (M10/M14/5/8-11), with cutting, grinding, and polishing accessories selected to match the workpiece and RPM rating.

Rotary hammer TCO is dominated by brush and chuck service, not sticker price: on a 1,000 hr annual duty cycle, brush, grease and SDS chuck rebuild routinely push lifetime cost 3-5x the initial purchase figure across SDS-plus and SDS-max classes.

Rotary hammer installation centres on matching chuck system, bit type, and hammer class to the substrate; pneumatic 0.401" shank tools (AIMCO, SOARTEC) suit vehicle/panel work, while SDS-Plus 26 mm concrete-rated electric units (1500 W, 730 rpm) dominate masonry anchoring. Size by weight, BPM, and C

Rotary hammers divide into corded, cordless and demolition-class machines, with chuck system (SDS-plus, SDS-max, hex) and impact energy (1.7–62 J) as the primary engineering classification axes per Bosch 2026 catalog.

Selecting a storage rack system comes down to four concrete decisions: pallet/SKU size and weight, throughput model (FIFO vs FILO), aisle width versus building height, and the load class your steel frames and beams must carry. Match those four to a rack type, then verify EN 15512 / EN 15635 / RMI co

Industrial work benches fall into five functional families — heavy-duty steel, ESD-safe electronics, mobile adjustable-height, modular workstation systems, and specialised laboratory benches — each defined by load class, worktop material, and frame geometry rather than by brand.

Aluminium mobile scaffold towers span US$100–US$800 per set on China-origin export listings, while EN 1004 class 3 EU units like the Munk 125111 list at €5,000. Total delivered cost is driven by working height, material, EN 1004 load class, and caster diameter.

Arc welding machine selection hinges on process family (SMAW, GTAW, GMAW, SAW), duty cycle, current type (AC vs DC vs inverter), and automation level, with 2026 OEM price bands from US$25-45 for portable stick units to US$3,000-7,000 for automated profile welders per Made-in-China listings.
Frame scaffolding selection is driven by load class, tube OD/steel grade, and coupler spec; current export price band is US$40–80/set with MOQ 50 sets from audited Tianjin suppliers (2026-05).
Steel mezzanine platforms list on Made-in-China at US$1.20/kg to US$190.63/m² across MOQ tiers from 100 kg to 100 m², with structural-vs-rack-supported systems separating a 5-10× material price spread for warehouse builds in 2026.
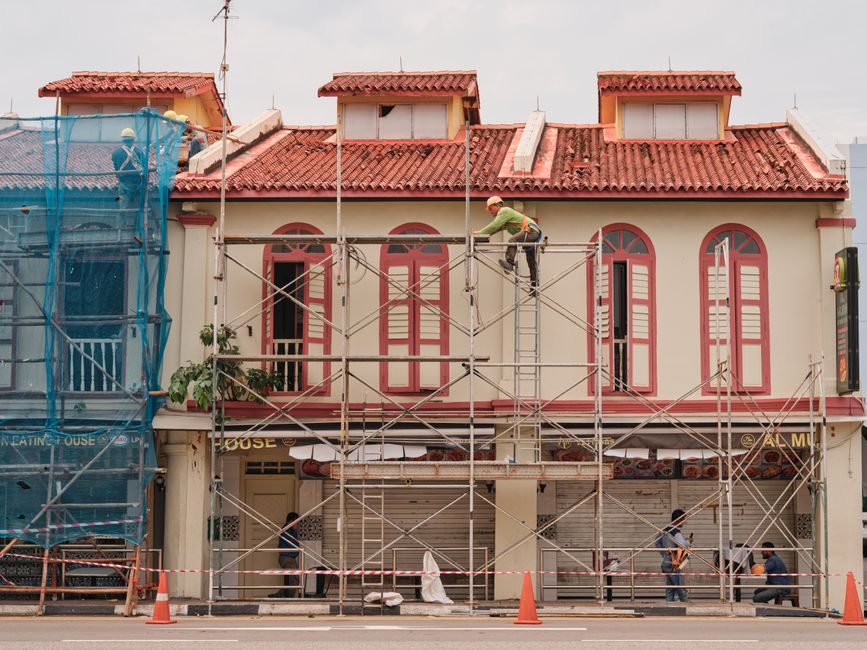
EN 1004-1 / DIN EN 1004 governs mobile scaffold towers; pick aluminium narrow-tower (e.g. SPEEDY, 0.58 m wide, 200 kg/m²) for indoor ≤7.1 m work, modular 1.80×0.75 m category-3 towers (3.35–13.20 m) for facade jobs.

Cuplock scaffolding lists at US$9–25 per piece on Chinese B2B portals in 2026, with galvanized top cups at US$0.40–0.50 and full systems Q235/Q345 at US$1,100–1,200 per ton; total cost depends on steel grade, surface finish, MOQ tier, and 81–90% export packaging routing.

Ringlock scaffolding (modular rosette system) lists at roughly US$3-17/piece on Chinese B2B platforms as of July 2026, with full-system packages around US$9-12/piece FOB Tianjin and 50000-piece weekly capacity; total project cost is driven by tube OD (φ48 vs φ60), steel grade (Q235 vs Q345) and surf

Ringlock modular scaffolding in Q235/Q345 steel with 48.3 mm × 3.25 mm tubes, hot-dip galvanized rosette verticals and aluminium scaffold planks at 2070/2570/3070 × 610 mm is the dominant modular access system for shipbuilding, stage and industrial maintenance in mid-2026.

Industrial hose reels span roughly $58–$199 per unit on Chinese B2B export channels (MOQ 50), with hydraulic and dual-hose industrial reels at $500–$585; US-built custom reels from Hannay are built-to-order in New York with a ~1-week ship window.

Mezzanine platform selection is driven by load class, structural support type, and the existing floor slab capacity: rack-supported, steel-structure, and free-standing layouts split 300-1000 kg/m² duty, with column grids of roughly 3-6 m anchoring layout decisions.
Industrial workbench FOB prices span roughly US$120 for light steel assembly tables to over US$1,200 for stainless-steel refrigerated units; selection pivots on load rating, top material, and bench-scale lab use.

Industrial work bench selection hinges on four quantifiable axes — load capacity (250–2000 kg), worktop material (steel/plywood/Bakelite/stainless), frame gauge (1.2–2.0 mm) and ESD/dissipative rating — none of which are captured in software "workbench" localisation guides that dominated search resu
Manual 500 lb double-scissor hydraulic lift tables list around US$309 retail, while 6-10 t hydraulic dock levelers sit in the US$1,500-2,500 FOB band and mobile platform trucks cluster at US$124-125 per piece MOQ 5 on China-made-in-China listings (2026-04 to 2026-06).
Hydraulic lift tables are scissor-actuated work-positioning platforms sized in 500-5,000 lb classes, with 23-39 in strokes and ANSI/EN 1570 compliance as the dominant spec gates. Selection hinges on capacity, lift stroke, lowered height, scissor count, and duty cycle rather than brand.
Industrial spot welding machine prices in 2026 span roughly US$415 for a manual bench unit to US$25100 for a 380V three-phase full-automatic resistance line, with kVA rating, weld thickness, automation class and servo architecture as the four dominant cost drivers.

Spot welding machine selection in 2026 hinges on matching kVA-class power, electrode force, weldable thickness (0.5–1.4 mm steel sheet baseline) and automation class to the workpiece; typical industrial spot welders range from 0 W control-circuit bench units to ~20 kW compacting heads.

Handheld fiber laser welders (1–3 kW) list at roughly $3,000–$14,000 ex-works for thin sheet-metal work, while automated battery-pack and robotic cells run $1.0M–$1.5M; TCO adds 10–20 L/min shielding gas plus lenses, nozzles and fume-extraction filters per Made-in-China and GWEIKE reference data.

For 2026 sourcing, laser welding machine selection turns on three concrete decision points: source type (fiber vs pulsed Nd:YAG 1064 nm), power class (75–2000 W), and sheet thickness range (0.3–12 mm). Match these against the joint stack — dissimilar metals, reflective alloys, and automation depth —
Pick a TIG welder by matching output current type (AC/DC vs DC), process mix (TIG/MMA/MIG), power draw (8 kW to 17.3 kW) and supply (230 V single or 400 V three-phase) to the workpiece; thin-sheet stainless and aluminum demand AC/DC pulse with HF start, tube production needs a dedicated automatic lo

MIG welding machine prices in 2026 split across three clear tiers: budget Chinese inverter units at US$200–225 FOB, mid-range European multiprocess inverters around US$1,500–3,000, and heavy industrial pulsed-MAG systems reaching US$9,000–70,000 when robot-integrated.
MIG welding machine selection hinges on duty cycle, wire-feed architecture, process set and shielding gas; entry-level 230 V inverter units suit 0.6–0.8 mm wire on 1–3 mm steel, while 400 V three-phase 9.5–15 kW synergic platforms cover 1.0–1.6 mm wire on structural and aluminium work.

Frame scaffolding on Made-in-China 2026 listings runs US$10–32 per piece at 50–500 MOQ for standard 1219×1700 mm H-frames, with galvanized mobile tower plank sets at US$15–25 and full ADTO frame-system packages at US$400–450 per ton; hot-dip galvanizing adds roughly 6–8% weight and 15–25% price over
Cuplock scaffolding built on 48 mm OD × 3.2 mm steel verticals with Q235/Q345 ledger material and EN 12811 certification is the dominant modular system spec from Chinese mills in 2026, with MOQ starting at 20 m.t. and monthly capacity up to 5,000,000 pieces.
Industrial storage rack system prices in 2026 span roughly $20 for light-duty utility shelving to several thousand dollars per bay for heavy pallet rack, with per-tier load capacity the dominant cost driver across retail, warehouse, and trailer-mounted categories.

Industrial storage rack selection hinges on five engineering variables — load per bay, fork-truck clearance, seismic zone, beam-to-upright engagement, and aisle-vs-cube ratio. Match rack class (selective pallet, drive-in, cantilever, mezzanine) to SKU profile, throughput, and ceiling height before a
Mining-grade arc welders cluster in the 300-600 A inverter class, with 200 A units covering light repair and 400-600 A MMA machines handling hardfacing and structural joints underground. Spec the duty cycle, electrode range and IP rating before the brand.
Arc welding machine selection in 2026 hinges on output current (120–500 A), duty cycle, electrode compatibility, and input power — inverter units dominate portable use while transformer AC sets still lead heavy fabrication.

Aluminum ladder selection hinges on duty rating (typically 100–150 kg), working height bands, step geometry, and EN 131-7 / OSHA compliance; 80 mm step depth and 3–8 step mobile platforms are the current spec sweet spot for industrial orders.

Aluminum ladders specified for chemical plants must use 6061-T6 or 6063 alloy, EN 131 / ANSI A14.2 certification, and fiberglass-reinforced plastic (FRP) treads where solvent splash or stray current is a known risk.
Aluminum ladder selection pivots on alloy grade, duty rating, working height and joint mechanism; match EN 131 / ANSI A14.2 duty class to site load and frequency, and verify rung profile, anti-slip foot and stabiliser spec before purchase.
Global suspended working platform supply splits between European safety-engineered OEMs (TRACTEL, Scanclimber, Safi, Sateco, ACCESUS) and a dense Chinese cluster in Jiangsu, Shanghai, Shandong and Hebei offering ZLP500/630/800/1000 series at aggressive price points. Selection hinges on platform leng
Suspended working platforms are modular rope-access cradles sized by length (typically 2-10 m), rated load (250-1000+ kg) and hoist climb speed (6-10 m/min); the 2026 sourcing base is dominated by Chinese OEMs offering ZLP-series and BMU-style units under EN 1808 / OSHA 1926.451 frameworks.

For data center facades and atrium maintenance, ZLP-series electric suspended working platforms (630–1000 kg rated load, 6 m standard cradle) are the dominant spec band; GEDA and FIMM are key European OEM benchmarks, Chinese suppliers dominate export volume per 2026-07 sourcing data.
Suspended work platforms (ZLP-series rope-suspended cradles) are specified by load class, platform length, hoist type, and EN 1808 / OSHA 1926.451 sourcing, with 250–800 kg payloads and 1–6 m modular lengths common across the 27-OEM global field tracked on 2026-06-08.

Auto-climbing formwork is hydraulic-rail formwork for high-rise core walls and bridge pylons: pour ~4-5 m per cycle, lift via rail-climbing shoes, select on pour height, wall geometry and crane independence.
Chinese scaffolding manufacturers now occupy roughly two-thirds of the global supplier footprint, with ISO-certified clusters in Qingdao, Nanjing and Jiangsu exporting EN 74, BS 1139 and EN 1065 Class D/E compliant systems at landed costs 20–35% below EU equivalents.

Chinese laser distance meter suppliers cluster around three manufacturing hubs: Nantong (Jiangsu) for trading-channel export, Changzhou (Jiangsu) for surveying-grade handheld units, and Chengdu (Sichuan) for OEM sensor modules, with FOB price bands from US$30 to US$85 on Made-in-China.com as of July

Pick a laser distance meter by matching range, accuracy and laser class to the job: industrial 240 m reflective units with SSI output for closed-loop control, 40-50 m portable units with angle measurement for layout, and Class 2 eye-safe designs for general site use.

Pick a laser distance meter by matching range, accuracy class and laser class to the job: handheld 40 m Class II units suit interior fit-out, 80-100 m models cover façade work, and 200 m+ surveyors are survey-grade only. Green-beam Class IIIa devices win outdoors, but cost roughly 2-3× a red-beam eq

Optical-mechanical theodolite J6e factory pricing on Made-in-China runs US$400-476 per unit; the same HKTDC sourcing taxonomy lists Theodolite as a standalone Photographic & Optical Equipment sub-category alongside Laser Range Finder and Prism.

Automatic level suppliers listed on DirectIndustry cover 16 manufacturers and 33 product lines as of 2026-05-22, with optical self-leveling and digital models clustered around Leica, GeoMax, Hi-Target and ComNav, while Made-in-China.com lists 20 automatic optical level suppliers with a low-end MOQ f
Automatic (optical/auto) levels are sized by working range 0.2-300 m, magnification 20-32x, compensator damping ±0.5-5 arc-sec, and IP54-IP67 housing, with two-axis vs single-axis tilt sensor and Bluetooth output as the 2026 differentiators.

For water-treatment tanks from 0.5 m to 12 m, ultrasonic automatic levels are the default pick: non-contact, IP67 probe heads, ±0.2–0.5 % of full-scale accuracy, and 4–20 mA + HART output. Capacitance and hydrostatic types cover foam, sludge and high-temperature digesters; guided radar handles aggre

Chinese OEMs dominate the global total-station supply base, with 200+ active makers on Made-in-China.com and Alibaba, MOQ-1 price bands starting near US$5,200 for non-auto units and US$8,000-9,000 for robotic/motorised CNC-class instruments, and 1,000+ prism/tripod/accessory lines from Jiangsu and S

Total station selection hinges on angular accuracy (1" to 5"), reflectorless range (typically 500–1000 m), and prism range up to 5000 m, with 2026 robotic models like the Topcon QS1A retailing near $5,980 USD per unit.

For oil and gas survey work, robotic total stations with 1 angular second accuracy, Class 1 laser safety, and IP66 sealing are the engineering-grade pick. The article ranks the leading spec bands a process engineer should demand when scouting plant layout, pipeline right-of-way and flare stack geome
China-based laser level suppliers cluster in Jiangsu, Shandong and Guangdong with 3-13 verified manufacturers on Made-in-China.com, Okorder, Tradewheel and HDLTools, offering 2-line to 16-line models at FOB US$0.05-54/pc with MOQs from 1 to 1,000 pieces.
Green-beam 510-530 nm self-leveling lasers dominate outdoor concrete and layout work; red 635-670 nm units still lead on indoor dry-wall runs. Choose by beam color, line count, accuracy, IP rating, and power source.
China-based floor grinder manufacturers dominate global B2B supply at US$650-1,050 for 220V/380V marble-concrete units, with Shandong and Guangdong the main clusters; key selection levers are voltage, disc diameter, and diamond tooling grade.

Portable gas-powered concrete groove cutters in the 14-16 inch / 50-65 cc class span roughly USD 250-500 list; blade diameter, engine displacement, and arbor size are the three sizing anchors spec writers must lock first.

Laser screed sourcing in mid-2026 is concentrated in China, with ride-on units listing FOB US$15,000-45,000 and small walk-behind units below US$5,000. Key suppliers include ROADWAY, Qingdao Pengfeng and Chongqing-based concrete-machinery exporters.
Mining-spec laser screeds are wide-format, hydraulically driven concrete placers built for slab pours exceeding 1000 m² per shift, with 4-wheel or track chassis, automatic laser or 3D GPS control, and head widths typically from 2.5 m to over 6 m for mill, warehouse, and haul-road workshop slabs.

10 ride-on power trowel makers across Allen, Bartell, Husqvarna lineups (S1) compete with 100+ China OEM/ODM exporters on Made-in-China listing on 2026-07-07; 36-inch walk-behind price floor hovers at US$ 1,200-1,360 retail and US$ 200/set FOB Ningbo at OEM tier.
China-based concrete vibrator makers dominate global B2B supply with FOB price bands of US$35–209 per unit across needle, shaft, surface and plate variants; 17–17,000+ employee factories in Zhejiang, Shandong and Ningbo regions compete on flexible-shaft experience, electric motor integration and exp

Internal concrete vibrators (30-50 mm shaft dia, 11,000-12,000 vpm, 0.75-2.5 kW) suit walls and columns 100-300 mm thick; form vibrators (3-15 kW, 6,000-9,000 vpm) handle >500 mm mass pours, with power frequency 280-300 Hz and amplitude 0.5-3.0 mm set by slump and rebar density.
Electroslag pressure welding (ESW) for rebar and structural sections is dominated by a tight cluster of Chinese OEM and ODM factories concentrated in Shandong, Hebei and Jiangsu, with audited-tier welding machine prices landing in a US$ 2,000–100,000 band per set as of June 2026 sourcing snapshots.

China dominates the rebar coupler supply chain: Shandong and Hebei clusters list threaded couplers from US$0.10–US$3.90/pc at 100–1,000 piece MOQs, with Cangzhou Bartech and Chiping Dingli among the most-cited audited manufacturers as of mid-2026.
Rebar coupler sizing pairs bar diameter (typically 12–50 mm) with a coupler type — parallel-thread, cold-extrusion, grout, upset-forged or weldable — each meeting splice strength per ACI 318 Chapter 25 and IS 16172.
China-cluster rebar straightener suppliers dominate global sourcing, with 4-14 mm diameter CNC straightening-and-cutting units priced US$2,600-3,300 at 1-piece MOQ and 7.5 kW drives running at 45 m/min for Φ4-Φ12 mm bar.

Rebar straighteners are not specified for food and beverage process lines; the industrial equipment that actually bends and straightens stainless round bar in hygienic plants is a stainless tube straightener or a sanitary-grade bar rounder running on 304/316L stock.
Rebar cutters fall into manual, hydraulic, cordless Li-ion, and electric bench classes sized to bar diameter from 4-32 mm; selection is driven by rebar grade (Grade 40/60/75), daily cut count, and jobsite power access.

Spec a rebar bender for water-treatment-plant reinforcement by matching bar grade (Grade 40/60/75), diameter range (commonly D10–D32 mm), mandrel radius (3d–6d per ACI 318), and continuous-cycle bending rate to the rebar schedule of clarifiers, filters and pump-station bases.
Air pick (pneumatic pick) sourcing on Made-in-China.com clusters around Hebei-based trading exporters offering chemical and industrial air picks; comparable pneumatic-tool categories such as air chisels, air riveters and air impact wrenches share the same Shijiazhuang-Taizhou supply belt with MOQs i

Air impact wrench supply in 2026 concentrates in Taizhou/Zhejiang and Ningbo clusters, with 1/2" and 3/4" drive models priced US$63-148 FOB and audited CE suppliers dominating export channels.
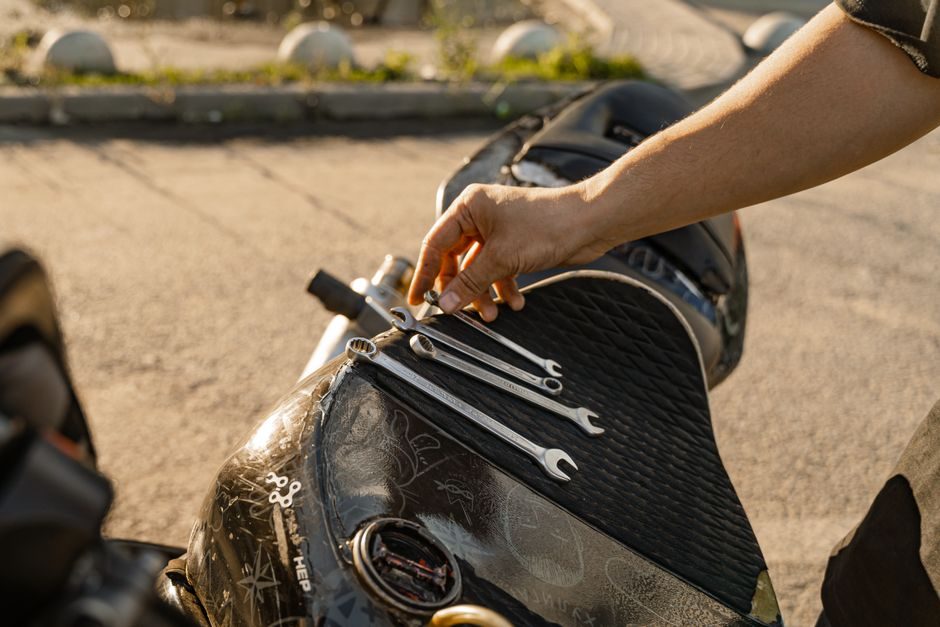
Air impact wrench sizing is driven by drive size, bolt capacity, max torque, air consumption and free speed; 1/2 in handles 200-900 ft-lb, 3/4 in 1,200-1,700 ft-lb, 1 in 2,000+ ft-lb at 90-115 PSI.
Pulp and paper mill maintenance crews typically need 1/2" or 3/4" drive pneumatic impact wrenches delivering 600-1,500 ft-lb of nut-busting torque with twin-hammer or pin-clutch mechanisms, paired with lubricated 90-120 cfm compressors and stainless or nickel-plated housings to survive moisture, bla
Pneumatic nail guns are sized by gauge (15-23), fastener length (typically 6-130 mm) and operating pressure (4.8-8.3 bar / 70-120 psi). Selection hinges on substrate, duty cycle and air-supply reality, not on the box label.
For aerospace interior assembly — aircraft seats, galley inserts, cabin monuments — the pneumatic nail gun is the wrong primary tool. Aerospace QA programs require controlled, repeatable joints via threaded fasteners, clecos, and structural adhesives; high-cycle nailing guns such as the Paslode F350

Match pneumatic nailer to fastener collation, length range and duty cycle: framing 21° Paslode F350 fires 2-4 in nails at 6/sec, finishing Senco F-18XP gives cordless pneumatic feel, coil CN70 handles 2-3/4 in fasteners.

Stud welder datasheets encode welding current ranges from 300 A to over 3000 A, duty cycle, stud diameter capacity, and capacitor bank rating as the four gates that decide which unit fits a given stud-onto-plate job.
Mining-grade power mixers are engineered around 4-8 m³ drum geometry, 30-75 kW drive envelopes, 2-3 m/s tip speeds and 25-35 MPa hydraulic circuits; selection hinges on ore-body abrasion, hoist weight and mill feed density rather than brand.
Power mixer selection on industrial lines hinges on four spec gates — viscosity ceiling, solids-handling, drive duty, and tank/agitator geometry — and the right answer changes sharply between low-viscosity blending and high-viscosity dispersion duty.
A demolition hammer is sized by impact energy (Joules), not watts or amps. Pick 11-16 J hex breakers for wall/chase work, 25-40 J class for floor and slab breaking, and 60-80 J hex/SDS-max for road and foundation demolition.
Zhejiang cluster dominates 110mm portable marble cutter supply; 1400W / 12000 rpm / 220V models ship factory-direct, while CNC bridge saws from Guangdong and Jiangxi cover stone-fabrication shops.
Chinese OEM clusters dominate circular-saw supply in 2026, with TCT blade blanks at US$50–143/piece and 250 mm wood/metal machines spanning US$630–25,200 FOB; spec the cut, not the brand.
Circular saw sizing is driven by three numbers: blade diameter, arbor/bore, and kerf matched to material density. Selection pivots on tooth count, tooth geometry, and body material (HSS, TCT, cermet, PCD) per application.
In power-generation field work, a 7-1/4 in (184 mm) corded circular saw with a 15 A brush motor spinning a 24-tooth carbide blade at ~5,800 RPM remains the default rig for cutting cable tray, Unistrut, sheet metal, and steel conduit; cordless 18-54 V brushless units now match that output for most ta
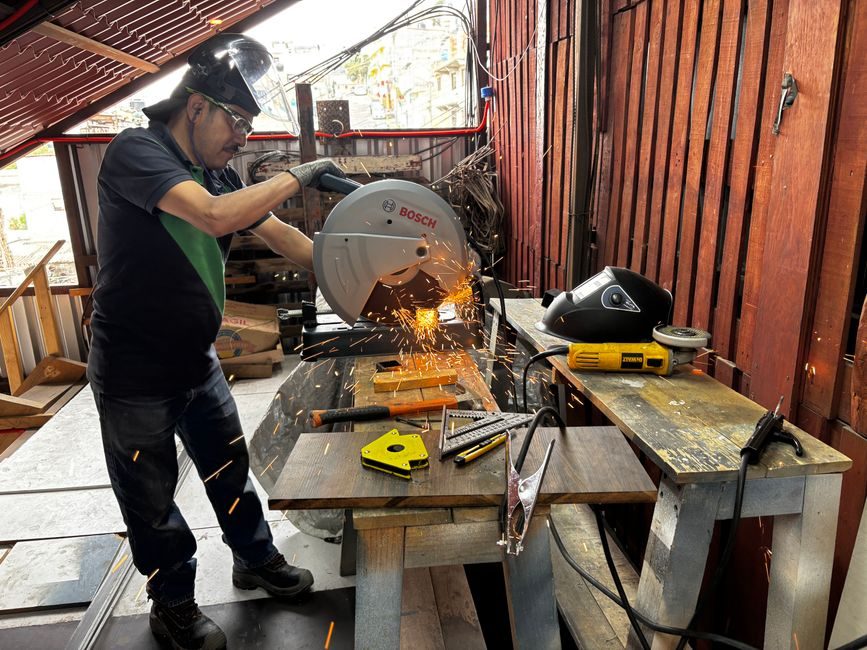
Industrial circular saw selection hinges on matching blade diameter, kerf, RPM and tooth geometry to workpiece material; stationary cold/cut-off saws dominate metal shops while portable units serve field carpentry.
China-based OEM impact drill manufacturing capacity is concentrated in Yongkang/Zhejiang and Jiangsu industrial clusters, with 13mm chuck corded models priced at US$11.41-17.40 FOB at 50-piece MOQ, and 30mm rotary hammer models up to 810W input power on offer as of mid-2026.
Aluminum ladder prices span US$15-2,000/set on Made-in-China in 2026, driven by alloy grade, working height, type (folding/telescopic/sliding), EN 131/ANSI certification and MOQ. Entry 4-step domestic ladders start at US$15.88; telescopic work platforms reach US$2,000.
Self-leveling 360-degree line/point laser levels now dominate 2026 pro-grade buying guides, with green-beam 4D models specified for indoor tile and drywall work and red-beam rotary units preferred for outdoor site layout beyond 30 m.
A 2026 rebar cutter buying decision runs on five gates: bar diameter, hydraulic or electric drive, cutting speed, blade reach, and total cost. Cordless 18-21 V models cover #4-#5 bar in 2.5-3 s, while 220 V/1050 W hydraulic units shear up to 40 mm rebar in under 5 s at 13-30 ton force.
A theodolite is the right tool for high-accuracy angle and traverse work over hundreds of metres, while a laser level is the faster, one-person choice for short- to mid-range horizontal/vertical plane setting on a typical construction site.
Automatic (self-leveling) laser levels in 2026 cluster into three line/color families — red cross-line (≤30 m), green cross/plane (≤45 m) and rotating/red beam (≤600 m with detector) — with prices spanning US$40 to over US$3,500 depending on accuracy class and IP rating.
Aluminum ladder selection hinges on matching alloy temper, duty rating (Type II 225 lb / Type IA 300 lb / Type IAA 375 lb), rung geometry, and EN 131-2 / ANSI A14.2 conformance to the worksite load and reach envelope; 6005-T5 / 6061-T6 extrusions dominate the 2026 supply base.
2026 retail prices for planetary concrete floor grinders sit between US$16,400 and US$26,400 for the Superabrasive Lavina Elite/Lavina S7 line; entry-level rotary floor renewing machines from Tianjin Kaida list US$2,500-US$4,600 per set on Made-in-China; abrasive consumables run as low as
For 2026 procurement, air impact wrenches are specified by drive size (1/4", 3/8", 1/2", 3/4", 1"), with 3/4" pro models delivering 550-1000 ft-lb max torque at 90 psi / 6.3 kg/cm² and 1/2" consumer models clustered around 1300 ft-lb. Match clutch type, free speed and air consumption to the fastener
Rotary, line, dot, and pipe laser levels each cover a distinct jobsite envelope; selection pivots on working range, self-leveling accuracy, beam color/visibility, and IP rating against published 2026 OEM catalogs.
SDC chucked 500 W corded rotary hammers on Made-in-China.com cleared US$12.50–63.80 per piece on 31 May 2026, while Bosch Professional rotates 18 rotary-and-demolition models through qualified dealers and SDS Plus consumables such as the DeWalt DW5478 7/8-inch bit list at US$26 on eBay
Suspended Working Platform selection hinges on seven spec gates: hoist type (LTD5/6/8), platform length 1.3–1.7 m increments, 200–300 kg rated capacity, suspension method, anchor rating, motor power and EN 1808 / OSHA compliance.
Stud welders in 2026 split into three process families — capacitor discharge (CD), drawn-arc (DA), and short-cycle — with prices spanning roughly US$1,880 for entry DA inverters to US$6,850 for 25 mm shear-stud sets.
FOB demolition-hammer prices on Made-in-China cluster at US$50-100 per piece at 100-500 piece MOQ for electric 1100-1500W hex/SDS-plus models in mid-2026, while full hydraulic excavator breaker sets land at US$3,999-5,000 per set FOB, with Makita HM1211-class OEM service parts topping out near US$13
Pneumatic nail guns drive fasteners in straight or angular collation at 70-120 psi working pressure; air picks deliver percussive chipping impact at similar pressure but no fastener feed. Selection hinges on whether the job is fastening or material removal.
Industrial sander factory prices span US$140-152 for used metalworking drum sanders to US$5,500-10,000+ for new wide-belt and desilter/desander units on Made-in-China, with orbital sanders concentrated in the brushless cordless segment.
For 2026 procurement, a circular saw buying guide is built around four gates: blade diameter and bore, drive power class, cutting material, and guide-system fit. Cordless 18V brushless rear-handle 7-1/4" units and corded 165 mm plunge-cut saws now bracket the prosumer range.
Parallel-thread rebar couplers in 45# carbon steel cover bar sizes D12–D50 with M12–M26 metric threads, 60°/75° thread angles, and 35–63 mm coupler length. Eight mechanical splice families (upset forged, cold-extrusion, grout, bar-lock, weldable, hex nut) compete on strength, seismic rating and bar-
Modular scaffolding systems from Chinese OEMs list at US$8.50–25 per piece for hot-dip galvanised ringlock/Cuplock sets in June 2026, with automated frame-welding cells at US$1,100–1,200 per ton. Scaffolding procurement is driven by steel grade, tube OD×wall, galvanising mass and order volume r
Rotary hammers and marble cutters overlap on Chinese OEM catalogues but differ fundamentally in impact mechanism, chuck type, and rated workpiece. A rotary hammer uses SDS-Plus/SDS-Max electro-pneumatic hammering for masonry, while a marble cutter is a diamond-blade angle grinder for stone, tile, an
Demolition hammers in 2026 split into three tool classes (light hex-chip, SDS-max, hydraulic) sized by joule impact energy, and a 1500 W SDS-max unit from Fixtec's 2026 catalog sits in the workhorse band most plant buyers actually order.
Sander selection in 2026 hinges on matching abrasive type, orbit diameter, dust extraction, and power source to substrate and duty cycle. Random-orbit sanders dominate finish work; belt sanders lead stock removal.
An impact drill is a rotary+percussive drilling tool rated 500–1500 W at 230 V/50 Hz with no-load speeds up to 3000 min⁻¹ and 13 mm chuck capacity, while a sander is a rotary or orbital abrasive tool designed for surface finishing only — they share no interchangeable function.
Total station procurement hinges on angular accuracy (typically 1″–7″), EDM range (often 500 m prismless to 10+ km with prism), and IP/operating-temperature class; motorised, scanning and robotic models dominate 2026 survey-tender specs.
An impact drill's job is to combine rotary cutting with a percussive hammer blow so masonry, concrete and structural steel can be drilled faster than a standard drill/driver. Buying decision is driven by chuck capacity, impact energy in joules, max RPM, hammer BPM and chuck type.
Concrete vibrators consolidate the slab internally while laser screeds strike the surface flat to ±3 mm over 6 m; the two machines solve different problems on the same pour, so contractors running slabs above 200 m² typically run both, not one or the other.
Arc welding machine selection in 2026 is driven by five spec gates: process type (SMAW, GTAW, SAW, GMAW), output class (amperage 160–500 A), duty cycle (35–60%), input power (single vs three-phase 380 V), and electrode compatibility (2.5–6.0 mm). Chinese OEM listings on m.ecvv.com and en.yiwugo.com
Infrared line levels typically trade at $23-$54 per unit FOB Ningbo for 500-piece MOQ orders, with 2-line/3-line self-leveling models dominating the 2026 procurement mix.
Marine stud welding on aluminum hulls and superstructures is dominated by drawn-arc capacitor-discharge (CD) stud guns with stainless 316L or monel studs, drawing 50-300 A at 50-200 V DC from inverter power sources.
Entry-level electric rebar threading machines start around US$980 per set FOB China (1-set MOQ), with mid-range hydraulic thread-rolling lines from US$1,799 and large GM350-class units supporting 20 units/month throughput; total landed cost is driven by motor class, roller count, and rebar diameter
Industrial air picks (pneumatic chisels) sourced from Chinese OEM/ODM factories in 2025–2026 typically list at US$30–180 per unit FOB, with heavy 1500 bpm chipping hammers reaching US$220–450; total landed cost adds 18–35% for duty, freight and consumables.
An automatic level in surveying is the optical/laser self-levelling instrument that establishes a horizontal sight line, with 2026 China-market complete kits running roughly CNY 700-12,000 based on optical/laser/electronic stage and brand tier.
Industrial 100 mm electric angle grinders sit in a US$30–60 retail band, 125 mm corded models US$50–150, and 125 mm cordless brushless kits US$120–320; total cost of ownership is driven by wheel cost, motor wattage, duty cycle, and IP rating.
An infrared line level in 2026 is a self-leveling laser line tool projecting a visible 635-660 nm line and a separate 850-940 nm IR beam for indoor alignment, with selectable accuracy bands of ±0.2 mm/m, ±0.3 mm/m and ±0.5 mm/m and 20-50 m indoor range. The right unit balances wavelength package, IP
Cut-off machine sourcing in 2026 maps to four OEM clusters: Zhejiang/Yongkang handheld abrasive saw makers, Anhui heavy-duty bench platforms, Italian/Swiss precision abrasive cutters, and re-branded Makita-compatible clones. Supplier shortlist hinges on wheel diameter class, motor wattage, and wheth

Floor grinder buying in 2026 hinges on power class (1.5-15 kW), disc configuration (single vs planetary vs HTC-style) and dust port size; epoxy prep kits and dust-port integrated units like the 220V Intbuying model define the entry band.
Impact drills land in three cost bands by 2026-06-24: $20-45 for 500-650 W consumer corded units, $55-110 for 800-1050 W pro-grade corded, and $130-260 for 18-20 V brushless cordless kits, with 230 V/50 Hz industrial models commonly quoted EXW at 3000-piece MOQ.
Impact drills in the 2026 export catalog cluster around 230 V mains, 800–1050 W input, 13 mm keyless chuck and 0–1100/0–3000 rpm two-speed gearboxes; 21 V cordless models sit in the 10 mm chuck, 16 N·m class. Match the chuck and the bit class, not the wattage number on the box.
Professional rotary and line laser levels span roughly $25 for entry-grade cross-line units to over $4,000 for fully automated motorised construction lasers, with mid-range self-levelling 360° models clustering between $300 and $900 as of mid-2026 retail listings.
Scaffolding and aluminum ladders serve overlapping but non-identical work-at-height roles: scaffolding wins on platform area and rated load per bay for facade and ceiling work, while aluminum ladders lead on portability, setup time, and tasks under 2 m on uneven ground. Spec selection pivots on reac
Angle grinder selection for 2026 buyers hinges on six spec gates: disc diameter (100/115/125/180/230 mm), rated input wattage, no-load RPM, spindle thread, switch type, and rated voltage — not brand. Map duty cycle first, then match guard, arbor, and dust port to OSHA 1910.215 / EN 60745-2-3.
Food-grade angle grinders are 304/316 stainless angle grinders, sealed dust-proof motors, 1000-1500 W input, M14 spindle, 11000 rpm no-load, used for hygienic weld bead removal and equipment surface finishing in food processing plants.
Rebar threading machines in 2026 are dominated by Chinese cold-rolling parallel-thread designs covering 16-40 mm bar at US$1,285-2,450 FOB Tianjin per set, with 15-second cycle times and 5.5 kW drives as the typical specification window.
New survey-grade total stations price from roughly US$1,200 for entry 2″ instruments to over US$18,000 for 1″ robotic GNSS-compatible models, with mid-band 2″/5″ mechanical units clustering between US$4,500 and US$9,500.
Selection of a pneumatic nail gun for wood framing hinges on four spec gates: nail length range 25-100 mm, working pressure 4-8 bar, magazine angle, and cycle rate above 60 shots/min, with 2026 EXW pricing clustered US$31-36 per piece at MOQ 1.
Total station buying in 2026 splits into a US$2,000-4,000 mechanical-encoder band (e.g. SOKKIA CX65 at $2,459), a US$4,000-15,000 reflectorless/servo mid-band, and a US$15,000-40,000+ robotic/IMU tier typified by SOKKIA NET05 AXII at $15,900, with angle accuracy, range and IP rating the main spec ga
Aluminum ladders in 2026 span 2.0-15 m working heights and 135-330 lb load ratings; pick between 6000-series, 7000-series, and 1xxx/3xxx tubing based on duty cycle, joint type, and standard.
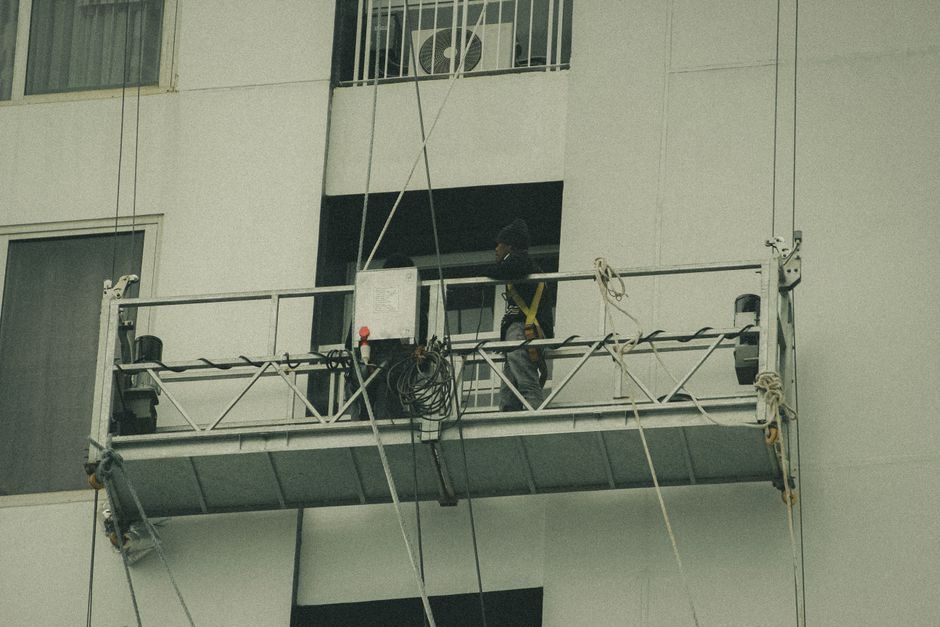
Aluminum ladders and suspended working platforms serve different heights: ladders (incl. mobile platform ladders) cap around 6-8 m for light-duty, single-operator work, while suspended platforms reach 50 m+ for facade crews, each with distinct EN 131/EN 1808 rule-sets.
Rebar threading machines cut parallel or taper threads on bar ends; rebar couplers are the mechanical splices that those threaded bars screw into. Spec the machine for thread length, RPM, torque and bar grade, then match the coupler to bar size, system type and code approval.
Air picks chip concrete at 1,500–3,500 BPM with low torque, while 1" twin-hammer air impact wrenches deliver 1,500–2,500 ft-lb of breakaway torque for M33+ fasteners — pick by material removal vs fastener torque.
Handheld laser distance meters under $30 cover 0.05–50 m consumer jobs, $200–$500 industrial units (Leica DISTO X3 class) push 0.05–150 m with IP65 and ±1 mm tolerance, and $5,000+ pulsed industrial rangefinders reach 3.5–5,000 m — selection hinges on range, accuracy class, laser class, and ingress
Rebar benders span roughly $150 for portable manual units to over $9,000 for 50 mm electric benders, with mid-range 25 mm models in the $1,200-$3,500 band. Sourcing from Chinese suppliers via Alibaba or Okorder typically yields 30-50% savings versus comparable Western brands, with MOQs starting at 1
Rebar benders and rebar cutters cover separate process steps on the same jobsite: benders form 90°/180° angles up to #6 bar, cutters shear clean up to 1-5/8" rebar. Combo units exist but force tradeoffs in capacity, weight, and motor duty.
Angle grinder sizing hinges on disc diameter (100/115/125/150/180/230 mm), motor wattage (500–2600 W), no-load RPM (6,500–12,000 min⁻¹) and spindle thread (M10 × 1.5 / M14 / 5/8-11 UNC). Match disc size to cut depth, duty cycle to material removal rate, and verify guard, disc and accessory max RPM e
Selecting an oxy-fuel cutting torch in 2026 hinges on plate thickness, fuel gas (acetylene, propane, MAPP, propylene, natural gas), nozzle bore matching steel grade, and oxygen pressure windows — a spec-first checklist that filters out unfit torches in under five minutes.
New 2026 theodolite price bands run from roughly $300 for 30x optical mechanical units to $14,000+ for 1 arc-second robotic total stations, with mid-range 5 arc-second electronic theodolites clustering around $1,800-$3,200.
Cut-off machines and power mixers are two unrelated tool classes sharing a 230V corded-power form factor but nothing else: a 14-inch 2300W cut-off saw drives abrasive or diamond wheels for metal/masonry, while a power mixer drives a paddle for fluids from paint to refractory castables. Spec gate is
TIG welder selection hinges on process mode (DC-only vs AC/DC), base-material thickness range, duty cycle at rated output, and HF/argon-purge control. Choosing the wrong combination burns thin aluminum or starves stainless chromium.
Arc welding machines in 2026 span manual stick inverters from US$100-class units to CNC stud welders at US$4,500-55,600 per set and fully automated gantry cells. Selection pivots on current rating (typically 200-500 A), duty cycle, process type and production volume, not on price alone.
Dry-mix shotcrete machines start near US$1,700 for mini electric units, mid-band rotor-type rigs sit at US$8,200-9,700 per set, and truck- or robot-mounted wet systems with 25-40 m³/h output reach US$125,000-350,000, with Chinese FOB pricing dominant as of mid-2026.
Entry-level single-phase DC TIG welders (140–200 A) list in the US$95–500 band on export channels, while 400 V three-phase AC/DC pulse units with water cooling sit in the US$3,000–8,500 OEM band as of 2026-06-18.
Rebar straightener 2026 price range runs from $850 for 1-6 mm light manual units up to $12,000+ for 6-32 mm servo production lines, with capacity (mm range), power source and roller count driving the total cost.
Handheld marble cutter FOB prices span roughly US$48-US$400 per unit on 2026 China-origin quotes, while bridge saws and 5-axis CNC centres sit in the US$8,000-US$80,000 band; the dominant cost levers are blade diameter, motor wattage, and CNC axis count.
Stud welder selection turns on four gates: stud diameter range, base-material compatibility, duty cycle and welding-process family. Match those first, then verify certification, gun weight and weld-cycle time before signing a PO.
Entry-level MMA/stick arc welders on Chinese B2B platforms cluster at US$ 350–620 per piece (MOQ 1) in 2026, while mid-power AC units sit at US$ 515–620 and higher-amperage 500 A inverter models are quoted at US$ 3,000–7,000 per set. Total cost of ownership is dominated by duty cycle, electrode cons
Rebar threading machine selection hinges on matching bar diameter range, thread profile, motor power and duty cycle to project rebar grade. Models like the GM350 cover 16-40 mm rebar for anchorage and coupler production.
Demolition hammers and angle grinders are different tool classes: demolition hammers deliver percussive impact energy (joules) for breaking concrete, while angle grinders deliver high rotational speed (rpm) for cutting and abrasive work.
Handheld laser distance meters in the 0.05–60 m class dominate the 2026 retail and trade catalog, with ISO 16331-1 accuracy, IP54 sealing and 2-4 mm typical tolerance separating contractor-grade units from toy-grade imports.
ZLP-series suspended working platforms from Chinese OEMs (Wuxi, Shandong) ship rated 500–1000 kg at 8.0–9.3 m/min with CE/ISO documentation, FOB Tianjin/Shanghai, MOQ 1 set, lead times 15–30 days as of May 2026.
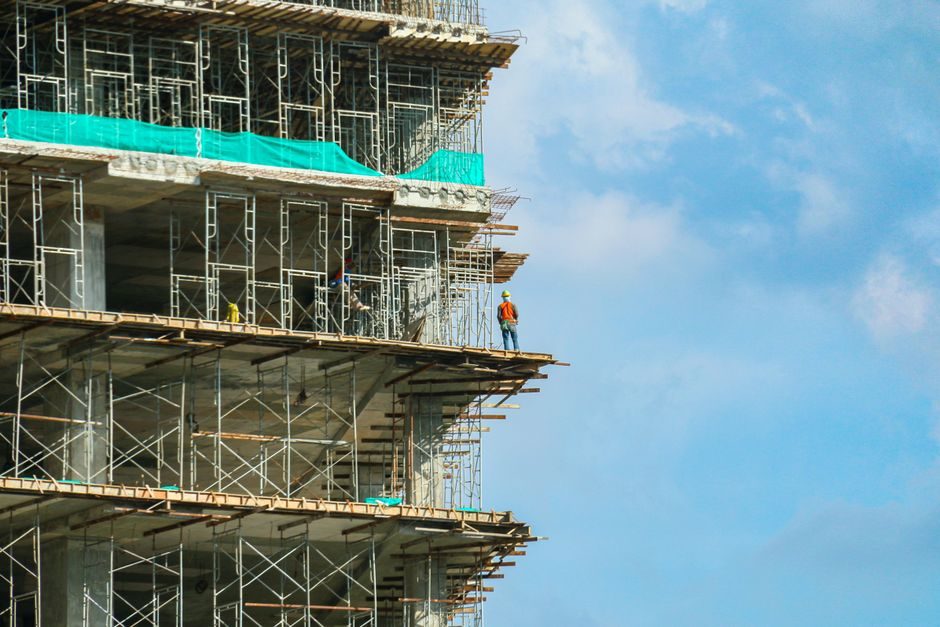
Climbing formwork is a load-bearing, formwork-attached platform system that climbs with the structure on hydraulic or crane lifts, while scaffolding is a separate access/support frame. Spec the former for shear walls, cores, piers and dam faces above ~15 m; the latter for facade access, soffit work
Mechanical rebar couplers and electroslag pressure welders join rebar on site through fundamentally different processes: a cold-worked mechanical sleeve that grips parallel threads versus a fused molten-pool weld in a copper shoe. Spec selection turns on bar size range, splice strength class, on-sit
Rebar cutter selection collapses to five spec gates — bar diameter range, rebar grade yield strength, power source, duty cycle, and blade replaceability — before any vendor or price comparison. Skip a gate and a 32 mm machine will bend instead of cut Grade 60 bar.
SDS-plus and SDS-max rotary hammers split the 2026 buying decision by bit-shank and concrete-anchor class: 2-4 kg corded models cover 6-26 mm bits for trim and M10-M16 anchors, while 5-12 kg breakers drive 16-52 mm bits in structural work. Brushless cordless 18-20 V platforms now match mains units o
Wet-mix shotcrete machines now dominate 2026 tunneling and slope-stabilization tenders, with FOB price bands of USD 6,000-39,000 and output rates of 5-30 m3/h defining the entry-to-mid class.
Entry-level electric wall chasers with a 1100 W motor and 2000 rpm no-load speed list around US $280-300 on B2C marketplaces, while a 16-inch 52 cc gas-powered concrete cut-off saw has been observed at US $294.95 with a 44% discount off a US $528.95 reference. Total installed concrete scoring and co
2026 wholesale pricing for handheld concrete vibrators spans roughly US$40-220 per piece at Chinese factories, with mid-range electric units clustering near US$130-150 and surface-vibrator specials at US$70-150. Drive type, poker diameter and shaft length are the three biggest cost levers.
ZLP-series suspended working platforms in mid-2026 export at roughly USD 1,200–3,800 per set FOB China, with cost driven by model (ZLP500/630/800/1000), aluminium-vs-steel deck, hoist power and CE/ISO certification pack.
Climbing formwork systems for vertical concrete construction in 2026 are sold as either crane-lifted (CB, SPF, M/L) or self-climbing/hydraulic (ACS, SCP) configurations, with indicative FOB ranges of roughly USD 65–210 per m² for aluminum frame systems and USD 1,200–3,800 per linear meter for full h
Rotary hammer sizing hinges on impact energy (J), chuck system (SDS-Plus vs SDS-Max) and application class; a 2-4 Joule SDS-Plus tool covers 6-16 mm masonry, while SDS-Max 8-20 Joule machines handle 20-50 mm concrete and chiselling.
Picking an angle grinder comes down to four hard spec gates — disc diameter (100/115/125/150/180/230 mm), input wattage class (500 W to 2600 W), rated no-load speed (typically 6600–12000 rpm) and spindle/thread fitment (M10 × 1.5, 5/8"-11 UNC, M14 × 2) — matched to the workpiece and the duty cycle.
A circular saw and a stud welder sit at opposite ends of the metal-fabrication toolchain: the first is a subtractive wood/metal cutting tool sized in blade diameter and RPM, the second is a joining tool sized in welding current and duty cycle. They share no working principle, no consumable format, a
Taylor Studwelding (UK) and Changzhou Qishuyan Jinda (China) remain the two anchor stud welder suppliers through 2026-06-25; Chinese drawn-arc units list at US$1,880-2,250 on Made-in-China.
A cut-off machine is selected by matching wheel type (abrasive vs diamond), drive power (1.5-15 kW typical), and arbor size to the workpiece material and section thickness, with swing-frame, chop-stroke, and CNC table formats each suited to distinct foundry, metalwork, and stone-cutting workflows.
Angle grinders and demolition hammers both run on 1100-1500 W-class brush motors, but the disc-driven grinder is a cutting/polishing tool, while the SDS-hex demolition hammer is a percussive chipping tool. The two machines share no usable output shaft and overlap on very few real jobs.
Angle grinder sourcing in mid-2026 is dominated by Chinese OEM/ODM hubs in Zhejiang, Jiangsu and Guangdong, with cordless 18-20V brushless kits and 100-230mm corded models at FOB-band US$32-260 per piece, MOQ 1-1000.
Rebar cutter pricing in 2026 spans roughly US $120 for an entry-level portable hydraulic RC-16 unit to US $950+ for cordless and AGQ-series machines, with the main cost levers being drive type, bar diameter capacity, and blade/cylinder build.
Air impact wrenches price from US$50 FOB for compact 3/8"–1/2" consumer units to US$480+ for new 1/2" composite pro models, with used 1" industrial wrenches from US$97–200 and 2-pack 1" sets shipping at ~18.4 kg.
Global rotary hammer supply is concentrated in Chinese OEM hubs, with 1,143 electric rotary hammer SKUs on Made-in-China.com and FOB price bands from US$30 to US$75 at 500-piece MOQ, while 8 industrial pneumatic/electric specialists list installation-grade units on DirectIndustry.
Cut-off machine selection hinges on matching blade diameter, motor wattage and duty cycle to workpiece material and section size. 355 mm handheld abrasive saws typically run 2200 W for steel profiles, while metallographic units prioritize low-deformation precision cutting.
Electric 230V internal concrete vibrators with 1.0–3.0 kW drives and 25–70 mm poker diameters are the 2026 workhorse for most slab and wall pours, with hydraulic and frequency-converter (high-cycle) units reserved for formed walls, precast, and large mat foundations.
Oxy-fuel cutting in 2026 still beats plasma on steel thicker than ~25 mm and on heavy plate up to 300 mm, with fuel gases (acetylene, propane, propylene, MAPP, natural gas) chosen by plate grade, thickness and local gas logistics.
Walk-behind power trowels sell between roughly USD 1,200 and USD 4,500 new in 2026 retail channels, ride-on trowels USD 18,000-USD 60,000, with engine power, blade diameter and clutch type driving most of the price gap. Spec the unit to the slab, not the brochure.
Power trowels 2026 span 24-inch walk-behinds for edge work to 46-inch ride-on units for 5,000+ sq ft slabs; China-origin ride-on trowels list US$3,300-3,500/piece, 36-inch pan packages sit at US$105-295/piece, and selection hinges on rotor type, engine tier, blade count, and operator certification.
Cut-off machine pricing in 2026 spans roughly US$35 for entry 355 mm chop saws to US$50,000+ for foundry swing-frame cut-offs, driven by blade diameter, motor power, automation and workpiece class.
Buying a theodolite in 2026 is a four-gate decision: angular accuracy (2″–10″), EDM range class, environmental rating (IP54–IP66), and data output. Match the gate profile to the job, not the brand sheet.
2026 TIG welding machine buying hinges on process match: AC/DC inverter (12,900–17,300 W, 230/400 V) for aluminum and stainless, DC-only for steel/copper, automatic seam units for 2–15 mm longitudinal work, with portable laser welders now crossing into thin-sheet territory at $3,600–$16,800.
Arc welding machines (MMA/stick) and TIG (GTAW) machines both use an electric arc but diverge sharply on filler handling, shielding gas, weld quality, and operator skill. MMA suits field repair on carbon steel; TIG delivers cleaner, more controllable beads on stainless, aluminium, and thin sections.
Infrared line levels and automatic (self-leveling) optical levels serve different job-site physics: infrared line modules project a fixed planar laser for short-range interior fit-out (typically under 30 m), while automatic optical levels self-level a telescope line of sight for outdoor surveying at
For 2026 site layout, pick a laser level when working range stays under ~300 m and accuracy of ±1.5–3 mm/10 m is acceptable; switch to a theodolite when sub-10-second angular accuracy, 1,000 m+ distance reads, or total-station data logging is required.
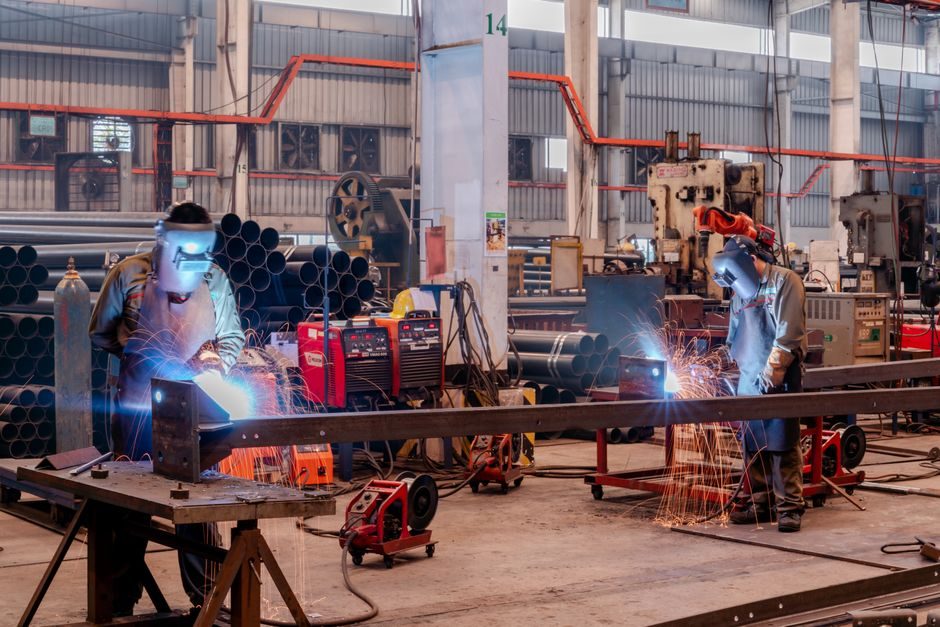
Entry-level capacitor-discharge stud welders list around US$3,500 per set on Made-in-China as of April 2026, while industrial stud welding consumables run US$0.03–US$0.22 per piece and full production lines span roughly US$7,000–US$30,000 once options, tooling, and welding controls are bundled.
Rebar benders in 2026 split into three form factors — portable hand-held hydraulic, bench/tabletop electric, and CNC production benders — with capacities from 16 mm (#5) hand-held units to 50 mm+ shop CNC machines. Price spreads $278 entry to $3,000+ for automatic stirrup lines, with 900 W–3 kW moto
Plasma cutter selection hinges on three spec gates — material thickness class, duty cycle, and cut quality tolerance — with consumable wear (electrodes, tips, shrouds) driving operating cost. Match power source amperage and CNC or hand-held format to job mix before quoting.
Rebar straighteners and rebar threading machines are separate production-line tools, not substitutes. Straighteners feed coiled stock at 3–6 kW and lengths of 500–6,000 mm; threading machines like the GHB22 work piece-by-piece on cut bars to roll parallel threads for mechanical coupler splices.
Circular saw prices span roughly $30 for a 10-piece diamond-blade pack to about $1,500 for a CNC sliding panel saw, with industrial TCT blades in the 350-500 mm range sized by diameter, tooth count and kerf width.
Air impact wrench selection pivots on square-drive size, nut-busting torque, free speed, and duty-cycle air consumption; a 3/4" drive twin-clutch model at 1356 N·m / 1000 ft-lb and 4500 rpm defines the heavy-truck benchmark from 2026 supplier listings.
Air pick selection in 2026 hinges on piston bore, stroke frequency, and air-consumption per stroke: handpiece mass below 1.5 kg suits underbody work, 2-3 kg covers panel beating, and rotary-hammer conversions handle 8-12 mm chisel loads. Match CFM, chuck type, and vibration class to the job before b
As of 2026-06-26, factory-gate rebar couplers in China and India cluster between US$0.20 and US$5.90 per piece depending on diameter, steel grade and certification, with 14-40mm threaded sleeves representing the bulk of B2B order volume.
A circular saw is a steel-disc power saw with peripheral cutting teeth that rotates on a spindle; selection pivots on blade diameter, RPM, kerf width, tooth geometry, and material compatibility for the workpiece.
Oxy-fuel cutting torch system price is driven by torch model, gas train and CNC class: portable kits land at US$25-2,500, mid-range CNC gantries sit between US$80,000-250,000, and heavy-duty steel-fabrication lines top US$2.5M.
Plasma cutter selection in 2026 hinges on cutting thickness (10-30 mm tier), current/amperage output, duty cycle, and CNC vs handheld configuration; China-made 5-axis gantry precision systems list at US$ 8,800-10,000 per unit on Made-in-China (2026-06), while compact CNC units run US$ 920-10,294.
Air impact wrenches and pneumatic nail guns share a compressed-air power source but diverge sharply on duty cycle, torque profile, fastener type, and exhaust management; 1" twin-hammer impact wrenches ship at 18.4-22.6 kg/4 pcs while F50B nail guns weigh 1.0 kg/piece, and that 18:1 mass gap is the c
Industrial power mixers span US$24–75 per piece at consumer/DJ tier, while heavy-duty planetary, sand, and concrete models from Chinese suppliers run US$1,000–30,000+ depending on motor kW, drum volume, and automation tier.
Rotary hammer is a percussive drilling/chipping tool using SDS shank bits, while marble cutter is a high-RPM abrasive disc tool for stone — two distinct machines, commonly confused on B2B catalogs. Choosing wrong risks tool damage and operator injury.
Rotary hammer selection hinges on five engineer-verifiable gates — chuck system, impact energy class, chuck-to-bit SDS compatibility, vibration control rating, and dust-port interface — before brand, price, or battery platform enter the conversation.
A floor grinder is a surface-prep tool that abrades hardened concrete with diamond tooling, while a concrete vibrator consolidates fresh wet concrete via immersed eccentric vibration — the two are not interchangeable and are specified at opposite ends of the slab's life cycle.
For automotive work, the best impact drill in 2026 is a 1/2 in cordless brushless model delivering 1,000+ in-lb (113+ Nm) fastening torque and a hammer-drill mode, sized 18 V or 20 V max platforms, matched with an impact-grade socket adapter set (1/4, 3/8, 1/2 in).
TIG welding machines and plasma cutters are separate processes, not substitutes: TIG joins metal with a non-consumable tungsten electrode, plasma cuts metal with a constricted arc. A combo unit is viable only for light fabrication; production shops still buy two dedicated machines.
Cut-off machine selection hinges on five hard gates: drive type (electric/pneumatic), blade technology, cutting wheel diameter, power rating, and swing frame geometry. Rotary-blade units deliver 60–80 m/s peripheral speed; portable 355 mm models ship at 2200 W.
Industrial scaffolding selection in 2026 is decided by load class (EN 12811-1 duty ratings), tube/steel grade, tie pattern, and the working environment — modular Cuplock, Ringlock, Kwikstage and tube-and-fitter remain the four live options for process-plant and EPC builds.
Portable electric rebar benders commonly cap at 25-32 mm bar diameter (single-bar) and 40-50 mm for shop-class three-phase machines, with the Fascut FR-800 rotary bender as a portable benchmark. Selection is driven by five gates: rebar grade (Grade 60/420 vs Grade 80/550), maximum bar diameter,
A rebar cutter and a rebar straightener are two distinct machines: the cutter shears bars to length (typical 4-16 mm capacity, 220V portable or 3-phase industrial), while the straightener removes coil set so bars feed into benders or cut-to-length lines with minimal strength loss. Specifying one for
Floor grinder selection hinges on four spec gates: power source (220V vs 380V), disc diameter (250-580mm), motor class (1.5-11kW), and dust port size (50/76mm), matched to substrate and site class.
Spec a pneumatic nail gun in 2026 by matching nail gauge, length range and firing mode to substrate: 18 GA brad models handle 5/8"–2-1/8" finish work, 21° framing nailers drive 2"–4" structural nails, while OEM framing units on Made-in-China.com sit in the US$11.50–36.00 FOB band.
A marble cutter and a rotary hammer are two distinct power-tool classes: the first is a 110-180 mm diamond-blade saw purpose-built for stone/tile scoring, the second is an SDS-Plus/SDS-Max percussive drill for masonry drilling and light chiselling. Cross-using one for the other's job produces bad cu
Climbing formwork selection in 2026 hinges on three axes: wall geometry (straight, tapered, circular), lift method (crane-jumped vs self-climbing hydraulic), and panel material (steel vs 6061-T6 aluminum). Frame systems suit low-rise; automatic hydraulic systems dominate high-rise corewalls above 80
Laser distance meters cover short-range one-person measurements to ~50 m, while total stations handle long-range, angle-resolved survey work past 1 km. Pick by range, accuracy and angle need, not by price alone.
Oxy-fuel cutting torches and arc welding machines serve different shop-floor jobs: oxy-fuel separates steel 0.5-250 mm thick by oxidation, while arc welding (GMAW, SMAW, GTAW) joins metal via a consumable or non-consumable electrode arc. Spec the right tool by thickness, joint type, material and req
Total stations deliver sub-2 mm angular + 1 km+ EDM accuracy for surveying and layout, while laser distance meters trade that precision for sub-3 mm range over 30-150 m in a pocket-sized body. Pick the former when control networks, traverses or stakeout require angle data; pick the latter for solo i
Angle grinder selection in 2026 hinges on disc diameter (115/125/150/180/230 mm), motor wattage band, and arbor size — match the tool to the workpiece, not the brand. Buy the smallest diameter that clears 80% of cuts.
Suspended working platforms and climbing formwork solve different access problems: ZLP cradles swing from roof rigs for envelope work, while auto-climbing formwork climbs the cast wall itself for corewall pours. Pick by structure type, cycle time, wind exposure and labour model.
A 2026 laser screed in ride-on or 3D form runs roughly USD 40,000 to over USD 250,000 new, with 4 m / 6 m walk-behind units at the low end and Somero-style 3D systems at the top; contractor rental and subcontract placement typically lands at USD 2 to USD 5 per m².
Handheld laser distance meters span roughly US$0.70–US$85 FOB China at 1-piece MOQ, mid-range industrial units run US$45–US$85, and premium 40 m units such as the Fluke 417D list around A$251, with sensors and pric
Shotcrete machines and power trowels sit on opposite ends of the concrete-construction toolchain: a robotic or wet-mix shotcrete unit pumps and projects concrete at 7-30 m³/h while a ride-on or walk-behind power trowel blades/finishes slabs at 90-180 rpm, with no functional overlap on a job site.