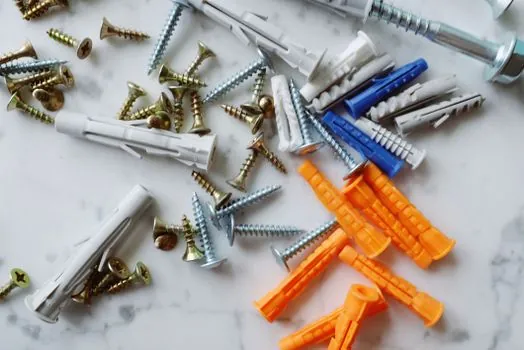
Mechanical expansion anchors are post-installed fasteners that grip cured concrete, brick, block, or masonry by deforming against the walls of a drilled, cleaned hole, and they remain the workhorse for securing machinery, pipe supports, overhead utilities, and baseplates in industrial facilities [S2]. The category includes three widely stocked sub-types, wedge anchors (external thread, integrated nut and washer), sleeve anchors (external thread, integrated nut and washer), and drop-in anchors (internal thread, set with a mating setting tool and used with threaded rod or bolt), and selection between them is driven more by load direction and base material than by raw tensile strength [S2].
Across warehouses, plants, and utility rooms, the same set of constraints recurs: cracked vs uncracked concrete, edge and spacing limits, embedment depth achievable with the available hole, and corrosion exposure from process fluids, washdown, or outdoor atmosphere [S1][S2]. Getting any one of those wrong turns a "commodity" anchor into a rework job, so the engineering work is mostly about qualifying the right sub-type and the right setting procedure, not about chasing the cheapest box on the shelf.
Wedge, sleeve, and drop-in: how the three expansion sub-types actually differ
Wedge anchors, sleeve anchors, and drop-in anchors all rely on mechanical expansion, but the way they transfer load and the way they fail under misuse is different enough that they are not interchangeable on a single drawing [S2]. Wedge anchors use an integrated stud, nut, and washer, and a wedge element that expands at the embedded end, making them the high-strength choice for cracked or uncracked concrete and the style most often listed for seismic, wind, and heavy baseplate loading [S2]. Sleeve anchors rely on a full-length sleeve that compresses around the bolt during tightening, which gives them better performance in brick, block, and softer masonry where the expansion point of a wedge anchor would simply punch through the wall of the hole [S2].
Drop-in anchors are internally threaded sleeves set flush with the concrete surface using a dedicated setting tool, so they are the natural pick for overhead applications, threaded-rod suspensions, and any location where a protruding bolt would interfere with traffic, covers, or future removal [S2]. Comparing the three on the criteria an industrial buyer cares about: wedge anchors win on raw shear and tensile capacity in sound concrete, sleeve anchors win on substrate versatility (concrete, brick, block, and hollow masonry with the right variant), and drop-in anchors win on flush-mount geometry and clean overhead installations, while all three share the same ceiling on edge distance, spacing, and minimum concrete thickness set by the manufacturer's design data [S2].
Substrate, cracked concrete, and the data the spec sheet must carry
The first technical question on any expansion-anchor data sheet is whether the published loads apply to cracked concrete, uncracked concrete, or both, since selection depends on cracked or uncracked concrete conditions, and any reduction in allowable load between the two cases directly affects design and qualification for the application. The second question is concrete compressive strength: most published design values are referenced to 2,500 psi (17.2 MPa) or 3,000 psi (20.7 MPa) normal-weight concrete, and going below that without re-deriving the numbers voids the design [S2].
Installation variables carry as much weight as the catalog number. Hole diameter is matched to the anchor (commonly 1/4 in through 1-1/4 in for the standard wedge-anchor range), hole depth is set to embedment plus a small clearance, and the hole must be cleaned with a wire brush plus compressed air or vacuum, because concrete dust left in the hole caps expansion travel and silently drops holding capacity [S2]. Engineers are also documenting setting procedure, torque value, and inspection criteria more rigorously than they did ten years ago, and the trend is reinforced by the broader move toward traceable, code-compliant fastening records on industrial builds [S1].
Seismic zones, fire ratings, and the qualification documents that gate the PO
Wedge anchors are the only one of the three expansion sub-types routinely carried with cracked-concrete and seismic qualification in mainstream catalogs, which is why they dominate structural-steel baseplates, equipment skids, and wind/seismic bracing in industrial facilities [S2]. Sleeve and drop-in anchors are typically used in non-structural and lower-risk applications, electrical supports, plumbing hangers, signage, and overhead utility suspensions, where the governing load is static rather than dynamic and where a seismic crack is unlikely to open beneath the anchor during the design event [S2].
Fire-rated assemblies add a separate layer of documentation: anchors embedded in fire-resistive construction need a listed fire rating (commonly 1- or 2-hour) supported by test data from a recognized lab, and that listing is what the Authority Having Jurisdiction (AHJ) accepts, not the catalog's generic "fire resistant" marketing line [S1]. Buyers in petrochemical and process-plant work also pull in corrosion-class considerations, with carbon steel zinc-plated suitable for dry interior service, hot-dip galvanized or mechanically galvanized for most outdoor exposure, and Type 304 or Type 316 stainless required for chemical, coastal, or washdown atmospheres where zinc would fail prematurely [S2].
Where expansion anchors are the wrong tool
Expansion anchors are the wrong fastener when the base material cannot generate the confining pressure the mechanism needs: hollow concrete block used as a shear wall, lightweight block below 2,000 psi, brick that is soft or old, or any substrate where the expansion force simply crushes the wall of the hole [S2]. They are also the wrong tool where vibration, shock, or sustained cyclic load would walk the anchor loose over time; in those cases a chemical anchor bonded with structural epoxy or a through-bolt with a backing plate is the engineering default, because the load path is bond or bearing rather than friction [S2][S4].
For refractory-lined vessels, kilns, and high-temperature equipment, traditional post-installed mechanical expansion is rarely the right comparison set at all: the question shifts to welded versus stud-welded refractory anchors, where stud welding wins on installation rate and weld consistency, and hand welding wins on positional flexibility and unusual shell thicknesses, with ceramic ferrule sizing tied to anchor diameter, shell thickness, and welding current [S3]. In overhead hollow-core plank or panel installations, drop-in anchors are usually replaced by through-bolts or specialty expansion anchor products listed for the deck profile, because a generic drop-in set into a thin web does not develop the published tension values.
Specifying the fastener: substrate, embedment, edge distance, and the corrosion class
A defensible expansion-anchor specification for an industrial facility pins down four numbers per location, and the rest of the data is housekeeping. Those four are: anchor type and diameter (for example, 1/2 in. x 5-1/2 in. wedge anchor), concrete compressive strength (minimum 3,000 psi at 28 days, normal-weight), edge distance (typically 6 to 10 anchor diameters depending on the product), and spacing (typically 10 to 15 diameters for full capacity, derated linearly as spacing shrinks) [S1][S2].
On top of that, the spec should call out the cleaning method (compressed air plus nylon brush, repeated per the manufacturer's printed instructions), the installation torque (printed on the anchor box and usually 30 to 90 ft-lbf for the 1/2 in. size, varying by embedment and product), and the corrosion class (zinc-plated carbon steel for dry interiors, hot-dip galvanized for outdoor, Type 316 stainless for chemical and coastal exposure) [S2]. Where chemical exposure is routine, buyers cross-check with the coating or fastener supplier because stainless grade alone does not guarantee compatibility with every process fluid, and the same engineering package typically also calls out the complementary industrial adhesive and chemical anchor systems used in adjacent baseplates or in rebar dowel repairs.
Installation productivity and the documentation trend changing the buying decision
Total installed performance, not the unit price on the box, is what is shifting anchor procurement on industrial sites. Manufacturers are responding with controlled-expansion designs that are more tolerant of hole oversizing, clearer setting-mark features that let the inspector see correct installation at a glance, and packaging that carries the ICC-ES, ACI 355.2, or equivalent evaluation report number in plain text so the spec writer can cite it directly [S1].
Adjacent digital tooling is starting to appear in the same workflow. Computer-vision and connected setting tools can flag drilling deviations, incomplete cleaning, or under-torqued installations before the load is applied, and AI-assisted design platforms are being used to organize load cases, substrate data, and spacing rules across a multi-discipline model, though the engineering community treats these outputs as drafting aids rather than substitutes for code-based approval [S1]. The net effect is that a buyer in 2026 expects a documented installation story alongside the steel: published cracked-concrete values, evaluation report number, torque procedure, corrosion data sheet, and a setting tool that the crew can actually use without damaging the anchor.
Trackable signals to watch over the next two quarters: continued consolidation of cracked-concrete seismic qualification into wedge-style products at the expense of sleeve and drop-in alternatives, broader adoption of stainless and hot-dip galvanized options as standard catalog SKUs rather than special-order items, and tighter integration of anchor design data with the same BIM and digital-twin models already hosting pipe-support and equipment-baseplate geometry. For related comparison work on bonded fasteners used in the same facilities, see the chemical anchor selection guide for school building projects, and for the dissimilar-metal corrosion issues that drive the stainless vs zinc-plated decision on adjacent baseplates, the adhesive selection reference for dissimilar metals covers the matching bond-line and galvanic-isolation criteria.