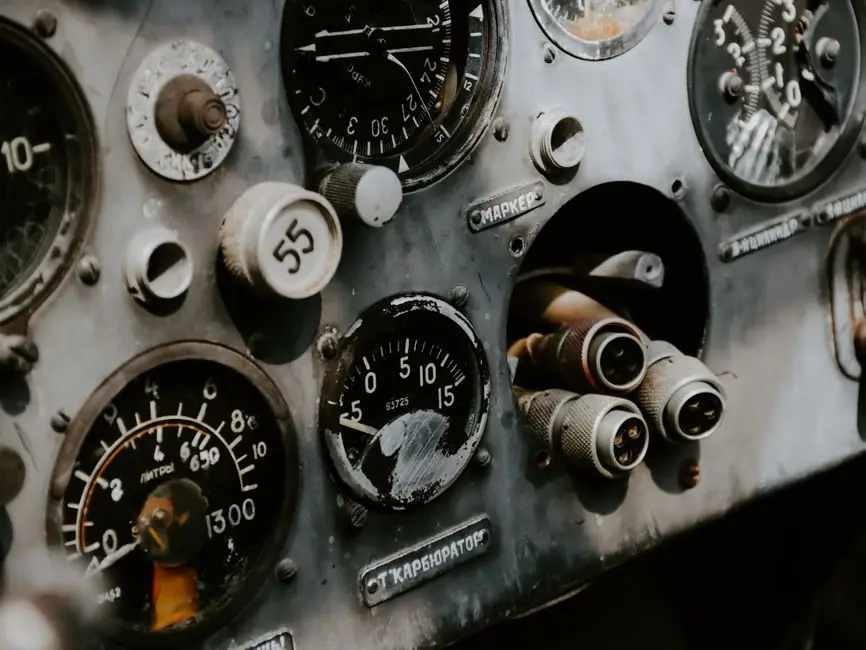
A dial indicator translates linear plunger travel into a rotational needle reading through a four-stage mechanical chain: a spring-loaded contact stylus, a rack-and-pinion converter, an amplifying gear train, and a graduated dial face, with typical resolution of 0.01 mm or 0.001 inch across a 1 inch (25.4 mm) standard stroke [S1][S4].
Inside the body, every 0.01 mm of spindle movement rotates the rack one tooth, which drives a small pinion that steps up through a gear train to sweep the main pointer across 100 graduations per revolution, while a smaller revolution counter (turn counter) records each full rotation of the main pointer for displacements that exceed one revolution [S2][S4]. The indicator is a comparison instrument: the operator zeroes the dial against a master reference (a gauge block, a known surface, or a spindle centerline) and then reads the difference between master and workpiece as runout, parallelism, taper, or height deviation [S1]. For background on the instrument family, see the dial indicator reference page.
The Four-Stage Conversion Chain, Stage by Stage
Stage one is the spring-loaded contact point (stylus): a hardened, replaceable tip that touches the workpiece and transmits linear displacement into the body under a controlled preload from a precision return spring, which restores the stylus to zero when contact is removed and maintains a consistent contact force across the measurement [S4]. Preload is set by compressing the spindle roughly 1/4 to 1/3 of full travel before zeroing, so the gear train is already engaged and any subsequent movement in either direction is read directly off the dial [S1].
Stage two is the rack-and-pinion: the linear motion of the stylus drives a small linear rack that meshes with a pinion gear, converting axial displacement into shaft rotation [S4]. Stage three is the gear-train amplification, where a second stage of reduction steps the pinion rotation up so that a small linear displacement, 0.01 mm in a standard indicator, becomes one full revolution of the large pointer [S4]. Stage four is the dial and pointer assembly: a graduated circular face with a calibrated scale and a rotating pointer, supplemented by a revolution counter that records full rotations for displacements beyond one revolution, so a 1 inch stroke indicator with 0.001 inch resolution and 0.100 inch per pointer revolution uses a smaller counter needle to track each full sweep of the main pointer [S2][S3]. The result is mechanical amplification: fractions of a millimetre the eye cannot resolve become sweep angles the operator can read directly.
Resolution, Range, and Least Count: How the Numbers Tie Back to the Gear Train
Resolution, also called graduation or least count, is the smallest division on the dial face and equals the linear input that produces one pointer graduation; standard workshop dial indicators deliver 0.01 mm (0.0005 inch) resolution, high-resolution inspection indicators reach 0.001 mm or 0.0001 inch, and the finest indicators go to 0.00005 inch [S2][S4]. Measuring range, in contrast, is the total plunger travel the body can accept: most dial indicators have a 1 inch (25.4 mm) stroke, long-range variants span 30 to 100 mm, and short-range high-resolution indicators cover only 1 to 5 mm because longer travel forces coarser gear pitch and coarser least count [S1][S3].
Accuracy on a quality dial indicator is usually equal to its resolution figure and is expressed as a plus/minus value, so an indicator with plus/minus 0.0001 inch accuracy displaying 0.0007 inch indicates a true value between 0.0006 inch and 0.0008 inch [S2]. Most 1 inch dial indicators use a 100-division outer scale plus a 10-division inner scale, with the main pointer reading 0.001 inch per graduation and 0.100 inch per full revolution, and the smaller counter pointer advancing one tick per revolution [S2]. Dial bore gauges, dial test indicators, and back-plunger indicators each use a different mechanical conversion path but rely on the same rack-and-pinion plus gear-train principle [S4].
Plunger vs Lever (Dial Test Indicator): Same Reading, Different Conversion
A dial test indicator (DTI, also called a finger indicator or lever indicator) uses a pivoting lever arm rather than a linear plunger, so angular displacement of the lever is converted into pointer rotation through a different internal mechanism, typically a sector gear or scroll cam that amplifies small arc movements [S1][S4]. The trade-off is range versus access: plunger indicators cover 5 to 100 mm of travel, while DTIs typically cover only 0.5 to 0.8 mm of equivalent linear travel, but the lever reaches into bores, under saddle overhangs, and onto lathe chuck faces where a straight plunger would drag or simply not fit [S1][S2].
For lathe spindle runout, the lever-type DTI is the correct tool, because a plunger cannot follow a rotating surface without scrubbing, while the lever sweeps tangentially with effectively no contact friction [S1]. Both families share the same reading convention: zero against a master, then read difference; the difference is which mechanical stage converts the input motion into pointer rotation. A direct comparison of the two families against workshop criteria is shown below.
Setup Discipline: Why the Mechanism Only Works in a Rigid Stack
The mechanical chain only delivers its rated accuracy when the indicator is mounted on a rigid stack, typically a magnetic base or precision stand, and oriented so the plunger is perpendicular to the measured surface; any flex in the base, any sideways load on the stylus, or any preload play will translate directly into pointer error [S1][S3]. For ring-and-pinion backlash measurement, the stylus must be aligned with the gear's rotation angle, the tip must rest square on the drive-side tooth face, and the pinion must be clamped or isolated so only the ring gear moves during the test, otherwise the backlash reading absorbs pinion movement and becomes meaningless [S3].
Two setup rules from the field cut most reading errors: (1) pre-compress the spindle about 1/4 to 1/3 of its travel before zeroing, so the gear train is pre-engaged in the direction the measurement will take; and (2) align the contact tip at 90 degrees to the surface being measured, since oblique contact introduces cosine error and lateral side-load on the rack [S1][S3][S5]. The bezel clamp behind the dial is then loosened to rotate the zero to the actual pointer position, locking the reference after the indicator is preloaded against the workpiece [S3]. For related metrology selection logic on adjacent instruments, the pressure transmitter reference page covers a different conversion chain (strain to electrical signal) that shares the comparison-measurement philosophy.
Reading the Dial: Counting Graduations, Revolutions, and Counter Ticks
To read a standard 0.001 inch resolution, 1 inch range dial indicator, the operator reads the large pointer against the 100-division outer scale for the sub-revolution value (for example 0.037 inch when the pointer sits on the 37th graduation past zero), then reads the small counter pointer for whole revolutions (for example 0.2 inch if the counter has advanced two ticks of 0.1 inch each), and adds them for the total reading: 0.237 inch in this example [S2][S3]. The same logic applies to metric indicators at 0.01 mm resolution with 1 mm per pointer revolution: read the main pointer to 0.01 mm and add the integer millimetres shown on the counter [S2].
Resolution finer than the graduation value is not readable, which is why high-resolution indicators (0.001 mm or 0.0001 inch) are physically smaller and have shorter range, since the gear-train ratio and the dial diameter together set the smallest visible sweep [S2]. Digital dial indicators replace the gear train and pointer with a linear encoder (optical or inductive) and an electronic display, but the underlying conversion, mechanical displacement to a displayed number, follows the same input/output chain, with the addition of RS-232 or USB output for SPC data logging, zero-set at any position, and min/max capture [S1][S4]. The Bluetooth-enabled digital indicator variant extends the same conversion chain to wireless transmission to inspection software, removing the operator-read step while preserving the comparison-measurement principle [S1].
Failure Modes and Calibration: Where the Mechanism Breaks Down
The mechanical chain has known wear points: the rack-and-pinion mesh develops backlash with use, the gear-train pivots wear and increase hysteresis, and the return spring loses calibrated preload over time, all of which show up as the same pointer returning to a different zero after a full-stroke cycle [S1]. Annual calibration against gauge blocks is the standard workshop practice to catch drift before it ships into a part, and any indicator that returns to a different zero after a full compression cycle, or shows more than one graduation of hysteresis at the same physical position approached from opposite directions, should be pulled from service [S1].
Common reading errors that masquerade as indicator failure include oblique stylus contact (cosine error, reads low), flex in the magnetic base or stand (reads high under load), preload set at zero travel instead of 1/4 to 1/3 (first 1/4 of stroke may not be in the linear gear-train region), and the tip riding on dirt or a burr (false peak in the reading) [S1][S3]. The mechanism is robust if the stack is rigid, the preload is correct, and the calibration is current, which is why the dial indicator has remained a workshop staple for over a century despite the spread of digital and laser alternatives. For an adjacent precision instrument whose accuracy class is similarly governed by a calibration interval, the OIML R60 load cell verification framework is a useful parallel and is covered in OIML R60 nmax and vmin: how load cell verification intervals are set.
Selection Rule of Thumb: Match the Gear Train to the Job
Match the indicator's range, resolution, and mounting to the specific measurement: choose a 0.001 mm high-resolution plunger with 1 to 5 mm range for toolroom and inspection-grade work, a 0.01 mm standard plunger with 25 to 50 mm range for general workshop measurement, a 30 to 100 mm long-range plunger for large-stroke alignment, and a 0.01 mm or 0.002 mm DTI for runout and bore-indicating tasks where access rules out a plunger [S1][S4]. Imperial users select 0.0001 inch resolution indicators in 0.025 to 1.0 inch range, with 1 inch being the US workshop default [S1]. The mechanism does not change between families: plunger or lever input, rack or sector first stage, gear-train amplification, pointer on a graduated face, revolution counter for extended range, and a spring to restore zero.
Two trackable signals to watch over the next 12 months: Bluetooth-enabled digital indicators continuing to displace purely mechanical workshop units in mid-tier inspection, and the AGD (American Gage Design) standard still defining the 3/8 inch stem and lug-mount geometry that virtually every plunger indicator uses for holder compatibility [S1][S2]. For a related discussion of how a different precision instrument, the flow meter, is selected against accuracy and range criteria, see pressure transmitter and the flow meter reference pages.