Exclude scheduled non-production time from planned production time, then include planned changeovers and maintenance as stop time within OEE.
OEE equals Availability multiplied by Performance and Quality, with the calculation anchored to the production constraint and supported by defined event codes.
Separate schedule exclusions from production stop time
Planned production time is the interval during which the asset is scheduled to produce. Time when there is no intention to run production is a schedule loss and sits outside the OEE denominator. Examples include a shutdown period outside the production calendar, scheduled non-working hours, and time when the asset was never intended to operate. OEE is applied only to scheduled production time, so removing these exclusions prevents a shutdown from depressing performance that was never planned [S2][S4].
That treatment differs from planned downtime occurring inside a scheduled production interval. Changeovers, planned cleaning operations, and preventive maintenance activities are examples of planned stops that may interrupt production.
Count every production-interval stop in the same place
Stop Time includes both unplanned stops, such as breakdowns, and planned stops, such as changeovers. Run Time is calculated as Planned Production Time minus Stop Time, and Availability is Run Time divided by Planned Production Time. Performance is then calculated as Ideal Cycle Time multiplied by Total Count and divided by Run Time, while Quality is Good Count divided by Total Count [S1].
The distinction is intent versus schedule boundary, not planned versus unplanned labels. If the process was scheduled to run but could not because no operator was available, the event is Availability downtime. If the same process was scheduled not to run, the interval does not belong in planned production time. Treating the first case as schedule loss hides an operational loss, while treating the second case as stop time penalizes the asset for time it was never intended to produce [S3].
Compare the main downtime treatments against four criteria
The comparison turns downtime classification into a boundary decision: exclude time outside the production plan, then deduct every stop that interrupts planned production. This approach supports direct OEE calculation without creating a separate score for calendar idle time. [S2]
Prevent planned labels from hiding excessive stop time
Planned stops such as maintenance, cleaning, inspections, and setup should be included in Stop Time. That preserves a clean distinction between a planned activity and an unplanned failure while still exposing changeover or maintenance inefficiency. A related calculation can be explored in SMED changeover reduction and the OEE math behind it.
Apply the calculation to real production events
The same principle applies to production demand. If the line is scheduled for 450 minutes but upstream starvation prevents output for 30 minutes, that event remains inside planned production time and becomes an Availability loss.
Control reason codes and edge cases
Reason codes need event-specific definitions. A production-window changeover should have a different code from a non-production shutdown, while an operator shortage should remain an Availability event. When planned downtime is 100% of the evaluated interval, Availability, Performance, and the resulting OEE value are undefined because there is no planned production time and no meaningful operating rate against which to calculate performance [S4].
Small stops can otherwise disappear from reports even though they consume production time [S5][S8].
Issue a written classification policy and audit it
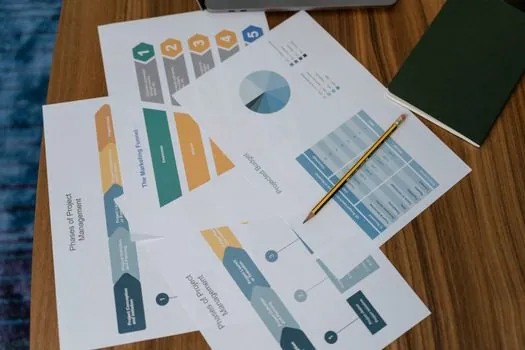
The production calendar should define planned production time, and every event should carry a start time, end time, event type, and reason code. Define planned changeover, planned maintenance, cleaning, inspection, setup, breakdown, operator shortage, starvation, and blockage separately. Also define the threshold between a minor stop and an availability stop, including the boundary treatment for events crossing that threshold. [S5]
Review the calculated result against two controls: the trend in OEE and the work-standard comparison for planned events. A falling Availability score may reveal increased breakdown or changeover time, while a stable score can conceal deterioration if excess duration has been relabeled as planned. The denominator must remain auditable, because any time removed from planned production time no longer affects Availability or OEE.
Track the count, duration, and excess time of events classified as planned, and compare them with approved standards each shift. If planned stop minutes rise while Good Count remains unchanged, the OEE record identifies a specific improvement target rather than an accounting adjustment.