Inline X-ray inspection detects casting voids, pores, cracks, and inclusions without sectioning, while battery systems screen internal cell structure at production-line speed.
The correct system depends on part geometry, material attenuation, defect size, image throughput, and whether rejection requires a radiograph, a reconstructed volume, or a calibrated measurement.
Choose Radiography, CT, or Manual Review by Decision Criteria
X-ray inspection is a non-destructive method for internal defects in castings, including voids, pores, inclusions, and cracks that can reduce strength, tightness, or dimensional integrity [S1][S4]. Inline radiography provides a practical balance between defect visibility, equipment complexity, and line speed, while cone-beam CT supplies depth-resolved information for difficult geometry and dimensional analysis [S2].
For a foundry handling mixed parts and moderate throughput, inline digital radiography is usually the first architecture to evaluate. For high-risk castings where crack orientation, location, or volume matters, CT is more defensible even when cycle time is slower.
Configure the System Around the Part, Not the Workbook
Castings may use sand, permanent-mold, die, gravity, investment, continuous, or pressure-die processes, with iron, steel, aluminum, copper, zinc, magnesium, titanium, nickel alloys, ceramics, and plastics among the possible materials [S4]. Part size, complex geometry, heterogeneous properties, governing quality requirements, output volume, and cycle time must therefore be resolved before choosing a detector, source, conveyor, or acceptance rule [S4].
For batteries, the mechanical envelope is equally specific. One listed pouch-cell system covers widths of 35–120 mm, lengths of 50–190 mm, thicknesses of 2–12 mm, and total machine lengths of 70–210 mm [S7].
Use industrial X-ray inspection to define the equipment scope, then validate source geometry, detector format, field of view, conveyor motion, and fixture clearance using representative production parts. A high-resolution image does not compensate for clipping, motion blur, poor part presentation, or insufficient material penetration.
Control Casting Defects Through the Correct Failure Mode
Voids are cavities or porous regions associated with trapped air and can impair casting strength and tightness, while pores are smaller air pockets that can reduce mechanical properties [S4]. X-ray inspection is appropriate when these defects are internal and the casting process or lot provides a credible statistical basis for screening [S1][S4].
Foreign inclusions such as sand, slag, or oxides create localized weakening, and cracks can form during casting or cooling and compromise part integrity [S4]. If a projection contains multiple dense regions or the crack orientation is unknown, do not force a 2D acceptance decision.
Misalignment, uneven cooling, incomplete mold filling, shrinkage, cold runs, and casting-skin defects can also appear as image or dimensional anomalies [S4]. Corrective action belongs upstream when the symptom is repeated at the same location or orientation, such as mold filling or cooling imbalance.
Recognize Battery Defects Without Confusing Them with Construction Features
Inline battery X-ray systems are used to detect hidden faults and analyze internal cell construction, but projection images contain both intended layers and unintended defects [S2][S5].
One inline pouch-cell configuration accepts parts 35–120 mm wide, 50–190 mm long, and 2–12 mm thick, with an overall length of 70–210 mm [S7]. Use these dimensions to screen fixture and shielding options, then establish acceptance criteria from known-good and known-defective production cells.
Automate Image Acquisition Without Removing the Validation Loop
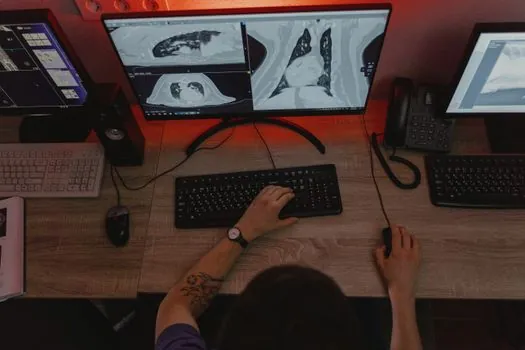
Automated inline and semi-inline X-ray inspection systems are used for critical electronic-component quality control.
A practical acceptance workflow has four stages: capture a stable image, apply calibrated defect logic, reject the part, and route rejected parts for review or retest. Monitor false calls, missed defects, cycle time, image reject rate, and review agreement separately. If a new alloy, casting coating, cell format, or supplier changes the image distribution, the existing model should be treated as unvalidated until it has been requalified.
For high-volume lines, compare full automatic radiography with semi-automatic radiography by part movement, operator intervention, average cycle time, image-review time, and defect segregation capability. Semi-automatic inspection is often the better transition path when stable automated recognition has not yet been proven. This is a process-validation decision, not simply a software preference.
Build a Defensible Performance Qualification
Qualification should use production-representative parts with known defects and record detection performance against defined defect sizes, locations, and orientations [S4]. For castings, include internal voids, pores, inclusions, and cracks that could compromise strength or tightness [S1][S4]. For batteries, include representative layered-cell defects rather than relying only on nominal cells [S2][S5].
Do not publish a minimum detectable size without recording the part material, thickness, source configuration, detector, geometry, dose, spatial resolution, and acceptance basis. A resolution figure without those conditions is not a usable equipment guarantee. Repeat the test after tooling, fixture, source, detector, recipe, or material changes, because each can alter the image relationship.
Radiation safety requires a site-specific program covering shielding, controlled access, interlocks, radiation surveys, and operating procedures. The referenced materials establish the inspection applications and automation functions, but they do not provide a radiation-safety standard, shielding calculation, or legal operating limit. Those items require project-specific engineering and applicable national regulations.
Separate Production Screening from Failure Analysis
Inline radiography is strongest when the process supplies repeatable defect populations and the decision is limited to accept, reject, or route for review. CT is stronger when internal geometry must be reconstructed, and metallographic or other physical analysis remains necessary when an X-ray indication must be tied to a specific material mechanism [S2][S4].
A frequent symptom is a rising reject rate after a line-speed increase. Check exposure timing, conveyor synchronization, fixture stability, part spacing, and image freshness before changing the acceptance algorithm. If blur or incomplete acquisition is visible, the corrective action is mechanical and timing control, not model retraining. If images are clean but indications persist, escalate the defect sample to CT, destructive analysis, or process engineering.
For mixed decisions between inline and end-of-line inspection, the broader method in Choose Inline Metrology or End-of-Line Inspection provides a useful starting point for matching inspection frequency to process risk and production economics.
The next verification step is to run a representative-part trial that records field-of-view coverage, cycle time, smallest validated defect, false-call rate, and CT escalation rate on the same parts before signing off the production recipe.