The labeling station is usually the last module on a packaging line and the one most often mis-specified, because buyers compare model numbers instead of matching the machine to the container geometry and label stock [S2]. For round containers the dominant choice is a self-adhesive wrap station, for square or flat bottles a flat-surface applicator such as the Primera AP550 handles rectangular, tapered and pouch formats [S1], and for sleeve-style decoration the choice narrows to shrink-sleeve tunnels fed by a sleeve labeler [S4].
Small-business buyers should measure container diameter and label height before comparing any model: those two numbers, plus roll diameter and core size, define the working envelope of every tabletop and mid-range machine on the market [S5]. For a selection deep-dive on the broader line context, see this capping and sealing machine sizing guide for the upstream torque and closure logic the labeler has to follow.
Step 1: Lock Down the Container and Label Geometry
Container shape is the first hard filter: round bottle, square bottle, flat bottle, special-shaped bottle, and hose labelers are distinct machine families in the beverage and personal-care trades, not options on one chassis [S4]. For flat surfaces, an AP550-class applicator covers rectangular, tapered, box, bag, pouch, lid and tin formats in a single platform [S1].
Label stock carries its own geometric rules. Self-adhesive film labels need a material thickness above roughly 100 micrometers to feed reliably; thin papers at 60-70 g/m2 are only workable as small price or shelf-edge labels because the release layer cannot hold them through high-speed peel [S4]. For irregular SKUs, dual-side or three-side machines exist but cost roughly 1.5x to 2x a single-side unit and need a longer conveyor [S4].
Step 2: Pick the Automation Band and Speed Envelope
Automation splits into semi-automatic and full-automatic, and then full-automatic splits again by container handling: linear conveyors dominate below about 150 containers per minute, rotary stars take over above that and run comfortably to 600 cpm on beverage lines [S4]. The first question to answer is whether your line actually needs full automation: manual tabletop units are still the right call for craft beverage, cosmetic, and specialty-food runs under roughly 30 cpm, because they trade throughput for setup time measured in minutes rather than hours [S5].
Speed claims need scrutiny. A linear self-adhesive labeler rated 30-150 cpm will drop to the lower end of that range on a tapered or square bottle because the orientation station becomes the bottleneck, not the label head [S4]. Buyers who ignore this often end up oversizing the dispenser and under-delivering on cycle time.
Step 3: Choose the Label Technology Family
Four label families compete for the same conveyor slot, and each constrains upstream choices. Self-adhesive (linered roll label) is clean, sanitary, and dominant in food, pharma, and cosmetics, with a release force set by adhesive type, silicone coating, and ambient temperature [S4]. Hot-melt glue labeling runs faster, is preferred for clear-on-no-label looks, and needs a glue pot heated to roughly 160-180 degrees C depending on the adhesive grade. Sleeve and shrink labeling delivers 360-degree decoration but adds a shrink tunnel and a steam or electric heat zone. Wet-glue (paste) labeling survives mostly in legacy beverage plants running returnable glass.
Self-adhesive label stock quality has three measurable gates: label firmness (governed by material thickness and area), release force (governed by adhesive and silicone), and base paper tensile strength with even silicone coating for sensor light transmission [S4]. A label that fails firmness will either skip the peel plate or be rewound with the liner; a label with inconsistent release force will either pre-dispense or stall. Both failures are mechanical, not software.
Step 4: Map the Production Line and Downstream Environment
Where the labeler sits in the line decides its in-feed and exit geometry. A labeler placed after a screw capper must be set back far enough to clear the capper star wheel, typically 600-1200 mm of straight-run conveyor depending on capper diameter [S2]. A line audit that ignores that gap is the most common reason a new labeler arrives and will not physically fit the existing layout [S2].
The product environment narrows the adhesive and facestock choices. Indoor ambient, outdoor UV exposure, freezer storage, oven heating, and chemical washdown each demand a different adhesive chemistry; a label that survives an autoclave will usually fail a -25 degrees C cold room [S2]. The same logic applies to the line environment: a wet bottling hall needs stainless 304 enclosures and IP54-rated control panels, a dry-pack hall can run painted steel.
Mainstream Options Compared Against Four Criteria
Self-adhesive linear labelers lead on changeover time (typically under 10 minutes for a SKU swap), hygiene (no glue or condensate), and label print quality, but trail on label cost per 1,000 and on the maximum decoration area they can lay flat [S4]. Hot-melt glue units lead on label cost (no liner waste) and on glass returnable economics, but trail on changeover speed and on sanitation. Sleeve-shrink lines lead on 360-degree branding and tamper-evidence, but add a shrink tunnel that consumes 15-25 kW and roughly 3-4 m of line length. Manual tabletop units lead on capital cost and footprint, but cap out around 20-30 cpm and depend on operator consistency [S5].
The numeric thresholds for shortlisting: if your run is under 5,000 units per month, manual tabletop pays back fastest. Between 5,000 and 80,000 units per month, a semi-automatic or compact linear self-adhesive is the usual answer. Above 80,000 units per month on round containers, a rotary self-adhesive or rotary hot-melt unit earns its footprint [S4]. For pouch, lid, or flat-carton SKUs above the same threshold, the flat-surface AP-class applicator scales further with a feeder conveyor [S1].
Who Should Not Pick the Mainstream Self-Adhesive Wrap
A self-adhesive wrap-around labeler is the wrong default in three common cases. First, very small diameter cylinders under about 25 mm often need a specialty small-diameter wrap head, because standard wrap plates will crease the label or skip the seam. Second, hot-fill lines above 85 degrees C need either a heat-resistant adhesive or a different label technology entirely, because standard acrylic adhesives soften and the label slides within minutes. Third, applications requiring tamper evidence should default to a shrink sleeve or a neck-band, not a self-adhesive body wrap, because the wrap itself carries no breakaway feature [S4].
Buyers running aggressive SKU changes (more than four label sizes per shift) should also avoid rotary self-adhesive units with fixed-size label drums, since each changeover can cost 30-60 minutes of line time. In that case, a servo-driven linear head with quick-change plates is usually the better fit.
Standards, Sourcing, and Machine Safety
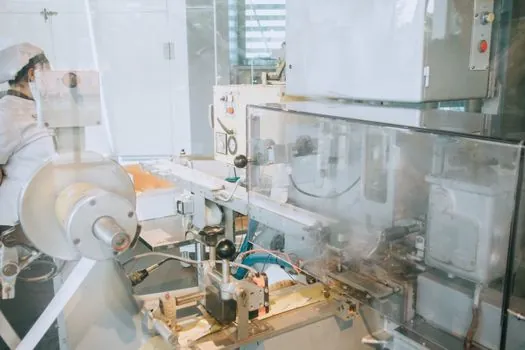
No single global standard governs labeling machines end-to-end, but several touch the integration points. Conveyor and guarding logic on automated lines typically follows ISO 13849-1 for safety-related control systems and EN 60204-1 for electrical equipment of machines, which is why a CE-marked labeler will arrive with a documented risk assessment. For food, pharma, and cosmetics contact zones, stainless 304 or 316 construction is the norm, with FDA- and EU 1935/2004-compliant elastomers and adhesives documented in the bill of materials. For packaging line safety logic more broadly, see the machine safety reference. [S4]
Sourcing works best as a four-step filter: define container and label geometry, define throughput band, define label technology family, and only then send a shortlist of two to three models to suppliers for cycle-time verification on your actual containers. This sequence cuts vendor-evaluation time by roughly half because suppliers who cannot meet the geometry or speed band drop out before a site visit [S2][S5]. For a fuller catalog view, the labeling machine encyclopedia entry covers the platform taxonomy.
Shortlist Logic and a Trackable Signal
Build the shortlist around the dominant container in your SKU mix, not the average one, and let the long tail of irregular SKUs drive a single flexible secondary machine rather than compromise the main one. Always test a vendor's claimed throughput on the worst-case container, not the round glass bottle they demo with, because that gap is where most projects slip their ROI date [S2]. A verifiable next node: request a 30-minute container trial on the candidate labeler using your actual bottles and labels, and ask for documented cycle time and reject rate over at least 500 units before signing a PO.
Component reference pages worth checking: coding machine.