Pinch valves isolate pharmaceutical product from the wetted valve mechanism, supporting sterile fluid paths in raw-material transfer, filling, powder handling, and finished-product duties [S2][S3].
Selection depends on chemical compatibility, pressure and temperature limits, internal and carryover volume, actuation response, cycle life, cleanability, and validation requirements, with internal designs commonly preferred where low dead volume and long service life are priorities [S5].
Define the valve duty before choosing a sleeve
A pinch valve controls flow by fully or partially collapsing a flexible sleeve, so the process medium contacts the sleeve rather than the actuating mechanism [S6]. This arrangement supports contamination control and a disposable or replaceable sterile fluid path, both central reasons pinch valves entered pharmaceutical processing [S2][S3].
Record each line’s fluid composition, concentration, temperature, pressure, flow range, cleanliness class, sterilization method, and allowable extractables profile before selecting a material. Sleeve options identified for pharmaceutical duties include natural rubber, EPDM, Viton, and PTFE constructions, but each must be checked against the complete formulation rather than selected by generic chemical family [S4].
Use the pinch valve reference for the general operating principle, then qualify the selected sleeve and body against the exact product-contact specification.
Compare external and internal architectures
External pinch valves clamp replaceable tubing and are easier to change, while internal pinch valves enclose the flow path and tubing within the port head, reducing maintenance and dead volume [S5]. The choice should follow the risk profile of the installation, not simply the purchase price.
The internal volume of an external or internal pinch valve is determined by the inner diameter and length of the tubing [S5]. Internal valves are the stronger choice when reagent loss, sample volume, carryover, and replacement labor dominate. External tubing remains useful when routine replacement, visual inspection, or a configurable tube path is more important.
Match flow precision and actuation to the process
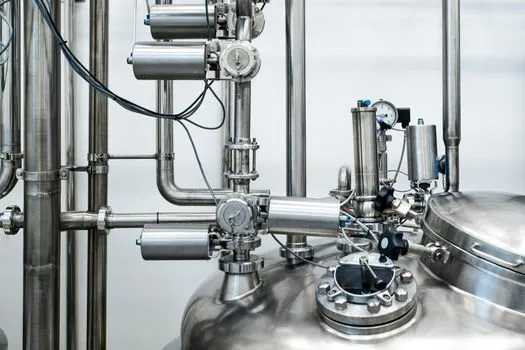
Two-way valves provide simple isolation, while three-way valves divert or flush flow but can trap carryover volume between the pinch point and the Y-shaped combination point [S5]. Proportional versions can regulate flow by varying sleeve compression, but control accuracy, response behavior, and cleanability must be confirmed with the selected actuator and valve body.
Electrically actuated pinch valves are used for sterile injectable filling, where the valve can maintain a disposable fluid path without the wetted motion of a piston [S3].
Solenoid actuation is common in medical and scientific pinch valves, with manual versions also available [S5]. For fast sequencing, compare actuator response, usable stroke, pressure signal, electrical load, and fail position rather than selecting by nominal “open” and “close” labels alone. Proportional duty also requires a defined minimum controllable opening, stable control characteristic, and acceptable accuracy across the operating pressure range [S7].
Check pressure, temperature, and sleeve reinforcement
The valve body, sleeve reinforcement, and pressure class must be selected together because an unreinforced sleeve may suit low-pressure service while a reinforced sleeve is required for higher differential pressure [S6]. Specify maximum allowable operating pressure at process temperature, not only the isolated-line pressure, because a closed valve can retain line pressure and actuate against it.
Sleeve material sets the practical temperature and chemical-compatibility envelope. Pinch valves avoid metal contact with the process medium, but elastomers can swell, permeate, or degrade under solvents and elevated temperature [S4]. PTFE-lined sleeves may suit demanding chemical service, yet the liner, reinforcement, and end sealing arrangement still require validation as one assembly.
For those services, a hardened or abrasion-resistant sleeve, controlled closure force, and suitable line velocity must be established through testing. For a broader technology comparison involving shut-off, slurry, and pressure duties, see Pinch Valve vs Ball Valve: Decision Matrix for Slurry, Pressure, and Shut-Off Service.
Design for aseptic cleaning and validated recovery
Connection type does not by itself establish aseptic suitability, so the selected assembly must support the intended cleaning route and preserve drainability.
Evaluate clean-in-place capability, drainability, crevice geometry, sleeve replacement, and whether the actuator permits complete sleeve collapse without trapping product [S2][S7]. For sterile processing, define whether the flow path is disposable, whether the valve can be sterilized in place, and which components contact the batch after cleaning.
Material evidence must be tied to the formulation and process conditions. Natural rubber, EPDM, Viton, and PTFE have different resistance profiles, and elastomer swelling, solvent sensitivity, permeation, and temperature-accelerated degradation remain specific qualification risks [S4]. The pharmaceutical angle-seat valve may offer another route for hygienic throttling, but a pinch valve is justified when contamination isolation, low internal volume, or replaceable sterile flow-path benefits outweigh its actuation and sleeve constraints.
Match the valve type to the intended use case
Pinch valves fit sterile filling, raw-material transfer, powder conveyor isolation, fluidized-bed or vacuum conveying, and applications where the product-contact surface must remain clean [S2]. They are particularly suitable when product contact can be limited to a replaceable sleeve and when no metal component needs to contact the medium.
Do not select the mainstream pinch valve when the duty requires a large continuous pressure drop, abrasive solids, very high temperature, extreme chemical exposure, or large-bore throttling outside the qualified sleeve envelope. Needle valves offer precision metal throttling and can handle some corrosive service better, but they introduce wetted metal, potential leaching, and a different cleanability profile [S4].
For sanitary isolation duties where the process requires a proven metal sealing stack, compare the pinch valve with a plug valve only through the actual product-contact and validation basis; the difference in contamination performance is not inferred from the actuator arrangement alone. In all cases, specify fill geometry, drainability, inspection access, and replacement method during the design phase.
Build the acceptance criteria before ordering
A pharmaceutical pinch-valve datasheet should state the valve type, connection, actuator, sleeve material, sleeve reinforcement, pressure class, temperature limits, flow coefficient or rated flow, internal volume, carryover volume, response time, cycle-life basis, cleaning method, sterilization method, and available compliance documentation [S1][S5][S6].
Set acceptance tests around the actual installation. For filling, include preheated dispense accuracy, repeated-stroke consistency, and recovery after cleaning [S3]. For sterile transfer, include closure integrity, residual-volume limits, drainability, and repeatability after thermal cycling [S2][S7]. For cycle-life qualification, compare the manufacturer’s 5-million-cycle or greater internal-valve basis with the external-tubing change interval of 200,000–500,000 cycles, then require a replacement plan [S5].
Close the purchase specification by reconciling the product-contact material list, sleeve compatibility evidence, operating envelope, calibration method, and maintenance interval. The final shortlist is simple: choose an internal aseptic design for low dead volume and long service life, an external design for replaceable tubing and field serviceability, and either type only when its qualified pressure, temperature, chemistry, and cleaning envelope covers the complete pharmaceutical duty [S4][S5][S6].