RV reducer quality is set by the tolerance stack on the cycloidal gear, the pin-gear, and the support bearings, not by gearbox assembly alone; the RV-40E virtual-prototype study shows transmission error responds directly to those three tolerance bands [S1].
For an RV-40E class unit (the representative mid-size frame for industrial-robot joints), the typical process chain is broaching of the cycloidal disc teeth, whirling of the pin-gear profile, grinding of the eccentric crank journals, and grade-selected rolling-element bearings; each station contributes a known share of the total transmission error [S1][S2].
Tolerance Design: Where the Transmission Error Actually Lives
The RV-40E study at Zhejiang University of Technology modeled the reducer as a tolerance stack with two parameters per part, bandwidth and position, and ran a virtual prototype across component combinations [S1]. The conclusion was operational, not academic: the cycloidal-gear tooth profile tolerance, the pin-gear pin-position tolerance, and the bearing accuracy grade together account for the bulk of the unit's angular transmission error, defined as the difference between the actual output angle and the theoretical angle at the same input [S1]. Optimized tolerance values landed close to what experienced engineers already specified, meaning the headroom for further tightening is narrow once the part is built to current production practice [S1]. For process engineers, the practical reading is that tightening the cycloidal profile without addressing the bearing grade rarely pays back in error reduction, and it always adds cost [S1].
Two manufacturing facts anchor the tolerance conversation. First, the cycloidal disc is almost always broached or shaved then finish-ground to hold the involute-curve profile; second, the pin gear is now commonly cut on a whirling machine, which holds pin-to-pin pitch within tighter limits than older turning-and-grinding sequences [S2]. When those two stations drift out of spec, backlash and torsional stiffness both move in the wrong direction, and no amount of bearing pre-load tuning downstream will recover the lost performance.
Standard RV-E Series: The Process Stations That Define the Cell
For a standard RV-E production line, the equipment set reads like a process map: a broaching machine for the cycloidal-gear internal teeth, a whirling machine for the pin gear, a grinding machine for the eccentric journals and the planet-carrier bores, plus a turning machine for the housing and end-cap interfaces [S2]. A laser-hardening or laser-cladding station is typically added to selectively harden the cycloidal-disc tooth flanks, because uniform through-hardening distorts the disc and burns the tolerance budget set in the prior grinding step [S2].
Four technical points are repeatedly called out for RV-E cells: cycloidal-gear precision, pin-gear accuracy, backlash optimization, and rigidity enhancement [S2]. The first two are tolerance problems; the last two are assembly and pre-load problems that the tolerance budget has to leave room for. If the cycloidal profile comes off the grinder already at the upper tolerance band, the assembly cell has no range left to set backlash by shim selection.
RV Reducers vs. Harmonic Reducers: Why Manufacturing, Not Geometry, Is the Differentiator
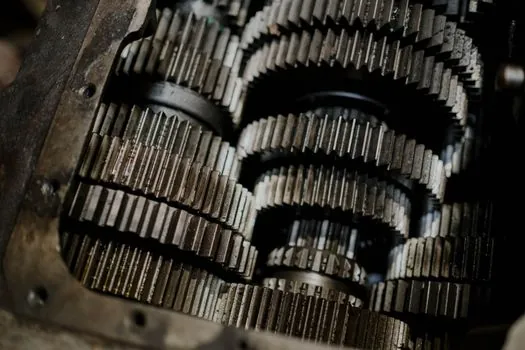
Compared to harmonic (strain-wave) reducers, the RV design's performance advantage comes from the manufacturing and assembly process stack, not from the basic gear geometry: RV reducers deliver higher fatigue strength, higher torsional rigidity, and longer service life under shock load, but only when the cycloidal profile, the pin gear, and the bearing stack are all held to their target tolerances [S3]. Harmonic units rely on a flexspline cup with a thin wall and a wave generator; their quality story lives in cup forming, heat treatment, and harmonic-curve grinding, which is a different process chain entirely [S3].
The trade-off for buyers is direct. RV reducers are the default pick where torsional rigidity and shock survival matter, which is essentially every six-axis robot waist, elbow, and shoulder joint, while harmonic reducers win in compact, lower-torque axes where zero backlash and small envelope matter more than absolute rigidity [S3]. Acceptance tests reflect that split: RV cells are typically gated on backlash in arc-min and rated torsional stiffness in N·m/arc-min, while harmonic cells are gated on transmission accuracy, repeatability, and lost-motion under light pre-load. The full RV reducer architecture and the alternative cycloidal reducer family share the same cycloidal-pin kinematic, so the tolerance lessons above transfer across both.
Selection Criteria and Acceptance Gates for Incoming RV Units
For incoming quality on an RV-E class unit, four numbers have to be on the inspection sheet: backlash at the output (typically quoted in arc-min, lower is better and 1 arc-min class is common in mid-size industrial-robot units), transmission error or transmission accuracy (also in arc-min, sets the robot's path accuracy), rated torsional stiffness (N·m/arc-min, the rigidity spec that lets the robot controller tune the joint), and no-load starting torque or running torque (the friction number that limits low-speed smoothness) [S1][S3]. Bearing accuracy grade is the upstream gate that locks the first three numbers into place; selecting a P4 or P2 grade bearing instead of the default P0 is the single most effective way to drive down transmission error without re-cutting the cycloidal gear [S1].
On the supplier-qualification side, the audit should walk the four stations in the same order as the process flow: broaching (cycloidal profile and surface finish), whirling (pin-gear pitch and roundness), grinding (eccentric journal and bore geometry, with cylindricity explicitly noted), and assembly (backlash set by shim or adjustable spacer, with torque checks at the no-load and rated-load points) [S2]. Skipping any station or accepting a wider tolerance band on a single station to ease supplier scheduling tends to surface later as drift in the field, not on the incoming bench.
Process Risks, Failure Modes, and What to Watch on the Shop Floor
The recurring failure modes on an RV line are predictable: backlash creep after a few thousand hours (usually a cycloidal-disc wear or pin-gear wear issue, traced to surface hardness below spec), vibration and noise at the joint (most often a bearing-grade mismatch, not a gear problem), and a step change in no-load torque (typically from eccentric-journal roundness drifting out after a grinder wheel dress cycle) [S1][S2]. Each of these maps to a tolerance band and a station, which is why the QA cell that owns the RV line should be organized by station, not by part number.
A practical engineering caution on cross-referencing: the cycloidal-pin principle used in an RV reducer is the same kinematic family as the broader gear reducer taxonomy, but the manufacturing tolerance budget, bearing grade, and pre-load logic do not transfer one-to-one to a standard planetary or helical unit. Specifying a planetary reducer in place of an RV where the cell design assumed an RV-style backlash and stiffness band is the most common line-stop the purchasing team has to unwind after a design revision.
Standards, Sourcing Signals, and What to Track Next
No specific ISO or JIS tolerance-class number for RV cycloidal gears is published in the research reviewed here, so QA sheets should reference the tolerance values and bearing grades on the part drawing rather than a standard number until the project team confirms the governing document [S1]. A useful external signal is how the aluminum key components and bill of materials spec rows survive the RFQ, because the RV housing, planet carrier, and end caps are typically machined from aluminum alloys, and the same alloy-grace and surface-finish discipline applies to those parts as to the cycloidal discs. For production-planning context, broader cutting tools demand 2026-2030 trends on broaches, whirling inserts, and CBN grinding wheels will set the lead-time and pricing for the next RV capacity expansion.
Two signals are worth tracking over the next two quarters: any published revision of the RV-E bearing-grade convention by major Chinese RV-E suppliers, and the first field data on laser-hardened cycloidal discs at 10,000+ hours, both of which will re-rank the four process stations above for buyers writing the 2027 RFQ. For now, the RV reducer tolerance, process, and acceptance gate story is the same one the RV-40E virtual-prototype study validated: pin the cycloidal profile, pin the pin-gear, and pin the bearing grade, in that order.