For inclines up to roughly 40°, integrally vulcanized chevron (V/Y) belts handle most bulk solids economically; once the design angle crosses 45° toward vertical, corrugated sidewall belts with T-cleats become the technically correct option [S2][S3].
Selection is driven by three engineering numbers: the conveyor's design angle, the material's angle of repose, and the largest lump size. The same belt conveyor frame can host either belt type, but pulley diameter, take-up length, and minimum transition geometry all change with the cleat/sidewall height [S2].
Incline Envelopes: Where Each Belt Type Works
Smooth fabric belts are generally reliable only to about 18–25° before the material's static angle of repose is exceeded and rollback starts, with troughed designs losing effectiveness beyond roughly 18° [S4]. A conservative rule of thumb is to design at ≤ (static repose − 5–15°), or about 0.8× the repose on risk-averse jobs [S2].
Chevron (V, Y, or herringbone) profiles extend the practical range to roughly 20–40° depending on cleat height and material [S2][S3]. Sinoconve's published chevron spec, dated 2026-09-17, quotes 20–40° as the operating envelope and lists cleat heights of 5 mm to 32 mm+ in standard patterns [S3]. Cleated-belt conveyor builders, such as Dorner, document a 60° ceiling for a generic cleated belt, but that figure typically assumes taller T-cleats rather than a low-profile chevron [S5].
Corrugated sidewall belts with T-cleats push the envelope to vertical (90°), because the corrugated sidewalls plus transverse cleats form enclosed pockets that mechanically retain the material column [S1][S2][S3]. Texas Belting & Supply documents custom sidewall heights from 1" to 16" (≈25–400 mm) and cleat profiles in I, T, lug, and angled shapes from ½" to 6" tall, matching the sidewall pocket geometry called out in BisonConvey's 2026-07-04 selection guide [S1][S2].
Cleat Geometry and Pulley Sizing
Cheveron belts use integral V-cleats, typically 15/25/32 mm tall in heavy rubber, with symmetrical open-cleat patterns that self-clean on the return run [S2][S3]. They sit on standard conveyor pulleys and do not require special transitions beyond the cover thickness.
Sidewall belts use hot-vulcanized attachments, with cleat heights from roughly 40 to 360 mm and sidewalls from ~60 to 400 mm, forming discrete pockets that are much taller than any chevron [S1][S2]. Because the sidewall is a flexible corrugated rubber wing, it must be supported through the return run by specially designed snub pulleys, and the minimum pulley diameter is set by both the base belt (ISO 3684 method) and the sidewall/cleat geometry; the larger of the two must win, or the cover cracks and the cleats fatigue prematurely [S2].
For lump sizing, the working rule is cleat height ≈ 1/2 to 2/3 of the typical lump for general bulk, and ≥0.75× the largest lump for sidewall pockets, so undersizing a chevron pocket on a 75 mm limestone run is a common field failure [S2]. A typical belt tensioner must also be sized for the heavier carcass of a sidewall belt, which is usually a multi-ply EP or NN construction rather than the lighter fabric of a chevron unit [S3].
Cost, Carcass, and Capacity Trade-Off
Chevron belts sit in the middle of the cost stack: more expensive than flat or generic cleated belts, but cheaper than corrugated sidewall, with integrally vulcanized cleats adding little to the splice or pulley budget [S6]. They are usually built on multi-ply EP (Polyester-Nylon) or NN (Nylon-Nylon) fabric carcasses rated for high tensile stress and impact loading [S3].
Sidewall belts cost more because of the corrugated sidewall extrusion, the hot-vulcanized T-cleat attachment labor, and the heavier carcass needed to carry the sidewall's vertical load. FEECO notes that steep-incline sidewall conveyors have slightly lower capacity than a flat troughed belt of the same width (18–72" belt widths are common for both) because the sidewalls consume part of the carrying cross-section [S4]. The footprint saving is the offset: a steep-incline unit can replace two belt conveyors and a bucket elevator, and an S-configuration steep incline can stand in for an entire transfer train, cutting transfer points and dust generation [S4].
For high-friction, lower-angle jobs (10–30°), a rough-top or wedgegrip belt on a standard flat belt carcass remains the most economical option, and it is the default in Texas Belting's incline/decline catalog, with FDA, oil-resistant, and anti-static cover compounds available [S1].
Selection Matrix: Chevron vs Sidewall by Criterion
Comparing the two on a fixed set of decision criteria gives a clear shortlist. The numbers below come from the 2026-07-04 BisonConvey selection guide, the 2026-09-17 Sinoconve chevron spec, the Texas Belting product catalog, and FEECO's steep-incline conveyor reference [S1][S2][S3][S4].
Maximum design angle: chevron reaches roughly 20–40°; sidewall reaches 45–90° (vertical). Cleat height range: chevron 5–32 mm+ standard, sidewall T-cleats 40–360 mm. Sidewall height: chevron not applicable; sidewall 60–400 mm (≈1"–16"). Relative cost: chevron is mid-tier; sidewall is the most expensive of the three common incline constructions. Carcass: chevron uses multi-ply EP/NN standard; sidewall uses heavier multi-ply with corrugated rubber sidewall hot-vulcanized to the base. Capacity at the same belt width: chevron is close to the flat-belt baseline; sidewall loses a small percentage of cross-section to the sidewalls. Minimum pulley diameter: chevron is set by cover and carcass (ISO 3684); sidewall is set by the larger of carcass and sidewall/cleat geometry. Best-fit material: chevron handles crushed rock, coal, grain, clinker, fertilizer, and bagged cement up to about 35–40°; sidewall handles the same materials plus ores, biomass, MSW, and wood chips where the lift requires 45° or steeper [S1][S2][S3][S4].
Use Cases and Failure Modes
Chevron is the right call for quarry and mining crushed stone up to about 35°, agricultural grain at 20–30°, and bagged-cement or clinker transfer where the lift is modest and a smooth idler transition matters [S3]. A 32 mm chevron on damp washed sand or slurry-coated ore is a common published recommendation because the open V-pattern sheds moisture and fines [S3]. The known failure modes are cleat wear at the return-side transition, spillage when material exceeds the cleat height, and slip-back if the design angle is pushed above the material's effective repose.
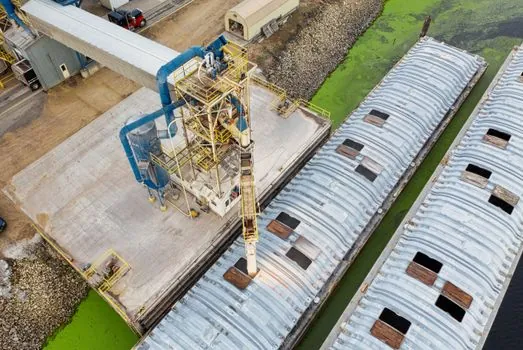
Sidewall with T-cleats is mandatory for 45–90° lifts: vertical bucket-elevator replacements, S-configuration steep inclines, mobile transfer conveyors at ports, and any application where footprint forces a steep rise [S1][S3][S4]. Failure modes include sidewall fatigue at the pulley if minimum-diameter rules are ignored, trapped-material buildup between sidewall and cleat if the cleat pitch is wrong, and splice failures at the sidewall/base-belt junction; cleaning access is also worse than on a flat belt, so belt thumpers and enclosed structures are commonly added [S2][S4]. For these installations, the take-up unit and belt tensioner must be sized for the higher steady-state load of a sidewall belt's heavier carcass.
Standards, Sourcing, and Spec Discipline
Cover grade and safety properties should be specified to the governing standards rather than by trade name: ISO 14890 for textile belts, DIN 22102 for abrasion, EN ISO 340 for flame resistance, EN ISO 284 for conductivity, and ISO 4195 for heat/ageing, where each property is required [S2]. Minimum pulley diameter is calculated by the ISO 3684 method, and the larger of the carcass- or cleat/sidewall-driven value is what goes on the drawing [S2].
The 2026 sourcing picture is that Texas Belting & Supply stocks rough-top, wedgegrip, V-cleat, and steepgrade belts from Houston for 10–45° duties, with custom cleated sidewall builds quoted on request up to 90°; Sinoconve's 2026-09-17 chevron catalog covers 20–40°; and BisonConvey's 2026-07-04 selection guide consolidates the cleat-height, sidewall-height, and lump-size rules used by the engineering community [S1][S2][S3]. FEECO's 2020 reference, while older, remains the clearest published note on how sidewall conveyor capacity compares to a standard troughed incline of the same belt width [S4].
Two signals worth tracking into late 2026: a wider shift from integrally vulcanized chevrons toward hot-vulcanized T-cleat/sidewall combinations as plants replace bucket elevators with single S-configuration steep inclines, and continued growth in 32 mm+ heavy chevron patterns for high-capacity aggregate and grain terminals where 40° is still acceptable.
Related analysis: Trapezoidal vs Curvilinear Timing Pulley Tooth Profiles: Spec Decision Guide.