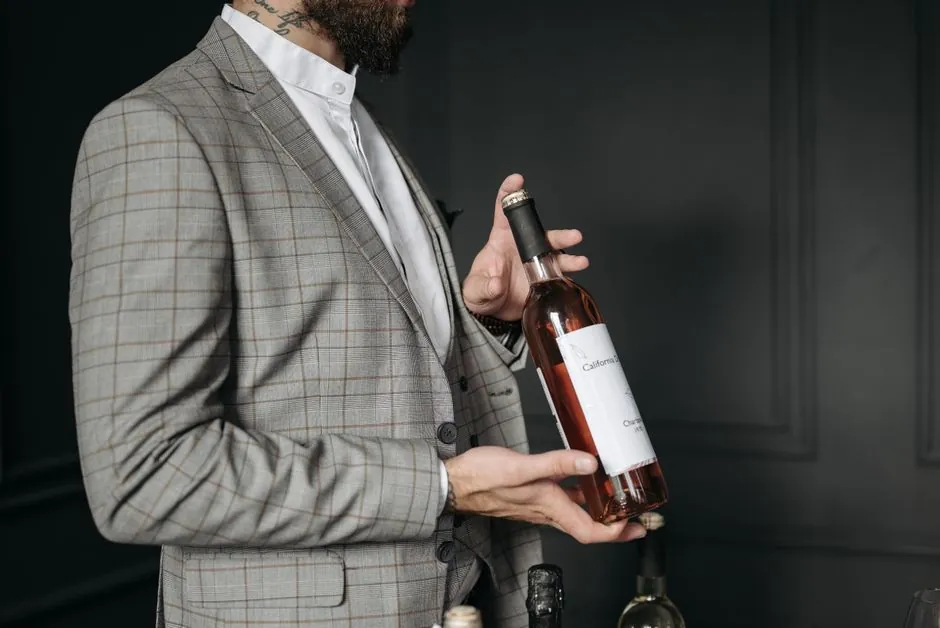
On a 750ml wine bottle, neck labels typically measure 1.5-3 inches wide by 0.5-1.5 inches tall, and the back label runs 3-4 inches wide by 3.5-4.5 inches tall [S5]. Front labels on the same bottle sit in a 3.5-4 inch square range, with the usable body panel rather than total bottle height setting the real ceiling [S1][S5].
Alignment between the neck strip and the front panel is governed by three physical relationships, not by artwork: the neck taper top and bottom circumference, the clearance between the label and the capsule, and the rotational reference relative to the front label [S2]. Get any one wrong and the bottle ends up with two technically correct labels that visually fight each other on the shelf.
Geometry Drives Label Size, Not the Artwork File
Wine labels live on curved glass, so the bottle family sets the panel first and the artwork adapts to it; a Bordeaux 750ml will accept a tall front label, while a Burgundy 750ml needs softer proportions because the shoulder transition changes usable height faster [S1]. For a 750ml Bordeaux the front runs 3.5-4 in by 3.5-4 in and the back 3-4 in wide; a slim 750ml Riesling drops to 3-3.5 in wide on both front and back, while a 1.5L magnum scales to 4.5-5 in square [S5].
Neck labels in particular are not just a shrunken version of the front: the neck's diameter and angle differ from the body, and the capsule leaves less usable height than a flat artwork screen suggests, so a 1 x 2 in to 2 x 4 in band has to be laid out against the actual taper, not a rectangle [S1][S2]. On curved or tapered surfaces, multi-panel alignment with the body label is one of the main complications a machine labeler has to handle, and it is the reason a hand-applied mockup often does not transfer to a production line [S2].
Three Relationships to Lock Before Approving a Die
The neck-to-front alignment problem reduces to three measurable gaps: the top and bottom circumference of the panel on the tapered neck, the clearance to the closure and any tamper feature, and the rotational plus vertical reference between the neck band and the front panel [S2]. Ignoring the first produces wrinkle, skew, or edge lift; ignoring the second pushes the label under the capsule or into the tamper band; ignoring the third is the most common cause of a bottle where both labels look fine alone but look mismatched together [S2].
On the body side, the back label is where compliance copy and producer notes live, which is why back labels trend slightly taller than front (3.5-4.5 in versus 3.5-4 in for a 750ml) and why the back width is the dimension that moves the most across bottle styles, from 3 in on a Riesling to 4.5-5 in on a magnum [S5]. Regulatory copy placement still varies by market, so the producer's compliance reviewer needs to sign off on the geometry, not the printer [S2].
Manual Application vs Machine Application, and Why That Changes the Spec
A small hand-applied run and a contract-bottler run of the same wine need different neck-label specifications, because the orientation tolerance a hand applicator can hit is not the tolerance a rotary neck station can hold [S2]. A semi-automatic L60 Tamp Rotary with a stepper-driven rotary and a bottle-specific clamping fixture, for example, can orient the label center with the front of the bottle, with a quick-change fixture for different bottle styles, and is rated for short-run liquor and wine work [S3].
For higher-volume runs, the R310 can apply a single wrap label or a front and back label to wine or liquor bottles at up to about 6,000 units per day for the average operator, using a tabletop mount, stepper-driven motor, and foot-switch activation [S3]. Where a die-cut pressure-sensitive strip has to be wiped down a tapered neck, a dedicated neck station with a folding tamp head and pneumatic fixture can run up to 40 products per minute on a square liquor bottle, which is a useful throughput benchmark for sizing the line [S3].
Material and Finish Choices That Move Alignment Tolerances
Thin films are commonly specified for beverage neck labeling because they conform to tapered glass better than rigid paper, which is one reason a paper mockup can look acceptable and a production roll can wrinkle on the line [S2]. For ice-bucket wines or anything that will see wet handling, a printed production sample should be tested after chilling and after a realistic wet cycle, because the same paper that looks aligned at room temperature can lift at the corners once cold and damp.
For bin and cellar-side tracking, the guidance is the opposite: label the location, not the bottle, because a paper label with no protection will not last a year in a damp cellar, while a laminated card or engraved tag will outlast the racking itself, and a pencil or grease pencil on a laminated card is the lowest-friction way to keep contents current as bottles turn over [S4]. Neck tags and other bottle-applied labels for cellar inventory are a poor choice for anything kept more than a few weeks, since the tag leaves the cellar the moment the bottle does [S4].
Sizing Comparison Across the Main Label Types on a 750ml
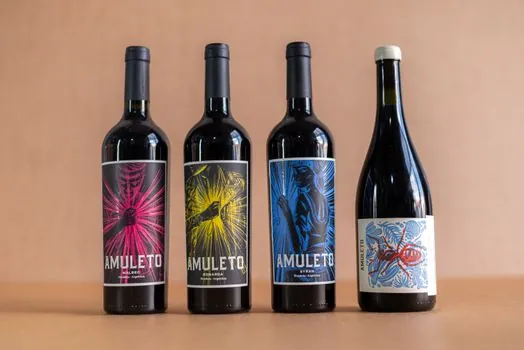
Using the 4over4 reference table for a standard 750ml bottle, the three label types sort cleanly on three criteria: panel width, panel height, and primary function [S5].
Front labels run 3.5-4 in wide by 3.5-4 in tall and exist for brand impact; back labels run 3-4 in wide by 3.5-4.5 in tall and exist for compliance text, tasting notes, and barcode; neck labels run 1.5-3 in wide by 0.5-1.5 in tall and exist as a foil- or capsule-adjacent accent that has to clear the closure and align rotationally with the front panel [S5][S1]. On larger formats, the same logic scales: a 1.5L magnum front and back sit at 4.5-5 in square, and a 375ml half-bottle front compresses to 2.5-3 in wide on both front and back [S5]. A practical bleed of 0.125 in on every side and a safe zone of 0.125 in inside the trim are the standard pre-press values cited for any of these sizes [S5].
Process Rules That Keep the Two Labels Aligned in Production
Sample with the exact glass bottle and capsule, not a drawing, and use an unprinted paper shape to confirm usable area before committing to a production-like printed sample [S2]. Photograph the front, side, and back of that sample, and check several bottles, not a single hero bottle, because the rotational drift between neck band and front panel is what the eye actually catches on a shelf [S2].
Ask the bottler how the package is held and oriented on the existing line, and whether a separate station or manual step is needed to apply the neck label, because the orientation a rotary station can hold is not the orientation a hand station can hold, even with the same artwork [S2][S3]. If a label wider than 4 in is specified on a 750ml, expect edge wrinkling, and on a 375ml half bottle the practical ceiling drops to about 3 in wide before the same failure mode shows up [S5].
Where This Breaks: Common Failure Modes and Limits
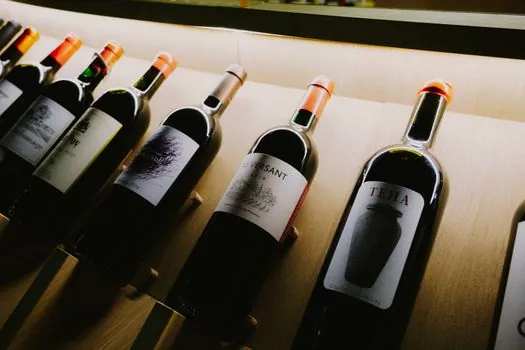
Wrinkle, skew, or edge lift is the failure mode when neck taper is ignored; unwanted overlap or a distorted edge appears when capsule clearance is wrong; and two individually correct labels that look mismatched on the bottle is the failure mode when rotational reference to the front panel is not locked [S2]. On the body, oversized labels cause wrinkles, drift through the labeler, and wipe-down issues on curved glass, and a label wider than about 4 in on a 750ml or 3 in on a 375ml is the practical wall where these start to show [S1][S5].
A useful signal for next month's run is to ask the labeler for its format limits and to request a trial on the actual bottle and capsule before approving the die and roll layout, because the geometry of the neck is its own package surface and behaves differently from the body [S2]. Track whether the contract bottler can hold neck-to-front rotational alignment at the line's rated throughput, since that single tolerance decides whether the band reads as a deliberate accent or as a misregistration on the shelf.
For component-level specifications, see construction machinery and equipment, lamps and light fittings, and lighting equipment and electric lamps.
For related coverage, see IEC 60073 pushbutton color codes: red, yellow, green, blue rules and exceptions.