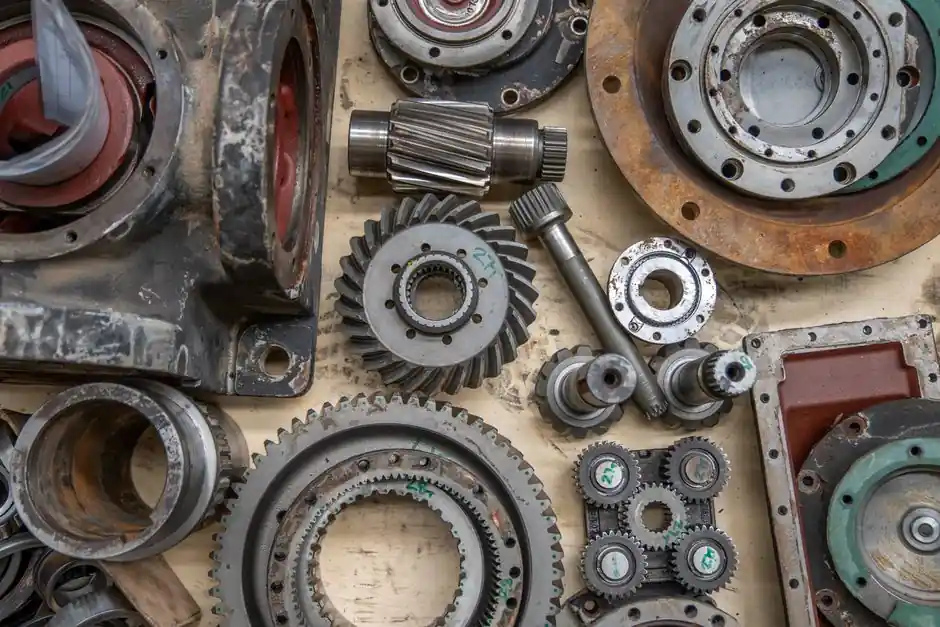
Aluminum high-pressure die casting dies typically deliver 75,000 to 200,000 shots over their useful life, with the spread driven by alloy chemistry, tool steel grade, part geometry, and maintenance regime rather than by machine tonnage alone [S2][S6]. A commonly cited benchmark is 100,000 cycles for aluminum cast at 1060–1220°F into H13 or DIN 1.2367 tool steel, while brass at 1640–1720°F drops to roughly 10,000 cycles from compounded thermal fatigue [S3].
The end-of-life trigger is rarely a single number on a counter; it is the first failure mode that pushes the part out of dimensional, surface, or process stability. Most process engineers now treat die life as a condition-based metric, not a calendar one. A standard HPDC production cycle runs 2 seconds to 1 minute, so a 100,000-shot die accumulates only a few hundred hours of actual injection time, yet absorbs tens of thousands of thermal cycles [S4].
Typical Die Life Ranges by Application and Process
For heavy-equipment structural castings on aluminum die casting machines, die life commonly lands between 50,000 and 200,000 cycles, with 100,000 cited as a typical midpoint for parts cast in H13 with verified heat treatment [S2]. Smaller consumer or electrical castings on the same machine class can stretch past 200,000 shots when geometry, slide count, and water-line balance are kept conservative.
Generic die-casting reference data places a single aluminum die at 75,000–200,000 shots over its life, with lead times measured in months and production volumes commonly quoted in the 10,000–1,000,000-piece band [S4][S6]. That range is broad because the dominant failure mode (thermal checking, gross cracking, erosion, soldering, washout, slide wear, cooling deterioration, or dimensional drift) varies by part, and the die's useful life ends when any one of these mechanisms forces the part out of agreed limits [S2].
Material, Temperature, and the Physics of Failure
H13 (DIN 1.2344) and DIN 1.2367 are the dominant die steels for aluminum HPDC because of their toughness, hot-strength retention, and resistance to heat checking at the 1060–1220°F injection window [S3]. Steel name alone does not guarantee performance; the verified heat treatment, grain direction at cavity surfaces, and section transitions set the real ceiling on cycle count.
Thermal fatigue is the binding constraint. The die surface sees a steep temperature swing each cycle: a hot shot of molten aluminum followed by water-mist cooling. Over thousands of cycles this cycling nucleates heat-check networks at cavity surfaces, radii, and thin steel sections, and the cracks can propagate into water lines or product surfaces [S2]. Running the die "colder" is not automatically safer: poor fill, large thermal gradients, and excessive spray can each introduce new failure modes faster than they suppress heat checking [S2][S7].
Soldering and erosion attack the cavity by a different mechanism. High-velocity metal stream erodes gates, runners, cores, and cavity details, while aluminum adhesion during ejection damages the surface and changes the release condition. Once soldering sets in, flash tends to rise as parting surfaces, locks, and slides wear, and the die's effective life shortens well before any heat check reaches a water line [S2].
What Shortens or Extends Die Life in Practice
Five inputs dominate: cast alloy temperature and chemistry, part geometry (projected area, section changes, deep cores, slides), gate velocity and intensification strategy, die temperature control (spray, water flow, warm-up, restart), and ejection/trimming force [S2]. Alloy family alone does not set life; a thin-wall housing in a magnesium-friendly tool steel can underperform a thick-wall automotive structural part in a well-supported H13 die.
Process levers that move the needle: balanced cooling channel layout, vacuum interfaces for high-integrity parts, replaceable cores and inserts at wear hotspots, surface treatments such as black nitride (which one commercial trial tied to reductions in scrap, downtime, maintenance, and cost of quality, plus more stable cycle and shot size), and disciplined warm-up/restart procedures to avoid thermal shock on cold starts [S2][S8]. Cycle time optimization is a related lever: every second shaved off the standard cycle multiplies into more shots per die per year, but aggressive cycle reduction without re-balancing cooling can crack the die through the cooler path itself [S1][S7].
Vacuum-assisted HPDC on a vacuum die casting machine is increasingly specified for parts where porosity tolerance is tight, and it indirectly extends die life by reducing gas-related soldering and post-cast welding repairs, though the vacuum seals themselves become a maintenance item with their own replacement cycle.
Comparison of Failure Modes vs Mitigation Levers
Eight mechanisms are usually responsible for end-of-life in aluminum HPDC dies, and each responds to a different lever [S2]. The table below lines them up against the most common mitigations a process engineer can pull:
Thermal checking at cavity surfaces: balanced cooling, verified H13 heat treatment, gradual warm-up; primary trigger, treated first. Gross cracking into water lines: section support, generous radii, controlled intensification pressure; usually a redesign, not a maintenance fix. Gate and runner erosion: gate placement, gate area sizing, replaceable gate inserts; commonly a wear-part play. Soldering/adhesion: release agent chemistry, surface treatment (black nitride, PVD), ejection timing; addressed in process and surface engineering. Flash growth: lock wear inspection, parting-line maintenance, slide rebuild; mechanical maintenance. Slide, pin, lifter, ejector wear: lubrication schedule, alignment checks, replaceable components; standard preventive maintenance. Cooling channel scale/clog/leak: water quality, flow verification, scheduled descaling; often overlooked until dimensions drift. Dimensional drift on machined datums: weld-repair protocol, post-repair stress relief, datum re-machining; metallurgy-controlled.
The takeaway: shot count is a meter, not a target. A die can still open and close while producing out-of-tolerance bearing bores, excessive flash, leak failures, or rough sealing faces, and useful life ends when the part fails its agreed spec at an acceptable cost [S2].
Maintenance, Inspection, and Cycle Counting
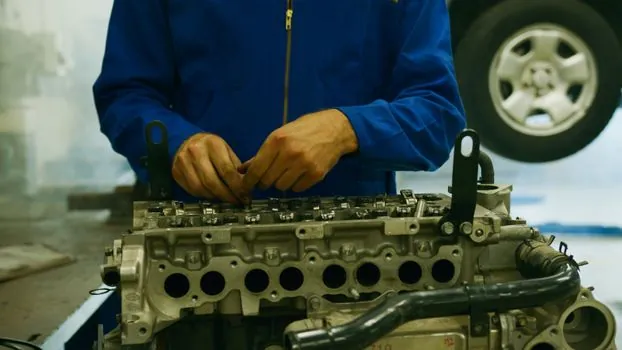
Condition-based maintenance beats calendar-based maintenance for HPDC dies. A practical inspection list covers cavity cracks, erosion, soldering, flash, ejector and slide movement, insert seating, vents, vacuum seals, cooling flow, leakage, hardness-sensitive repairs, dimensional trends, and surface state, with photographs, crack maps, dimensional trends, shot count, and process history kept in a single log [S2]. Inspection frequency should rise where failure consequences or measured trends justify it, not where the calendar turns over.
Replaceable cores, inserts, gate elements, wear plates, and slide components are the structural reason large structural dies can reach the upper end of the 75K–200K band. They preserve the main die investment by moving wear to cheaper, faster-to-replace parts, and they make economic sense when the parent die is built around replaceable sub-assemblies rather than monolithic features [S2].
For shops running die casting machines at 1,600–2,000 tonnes of clamp force for large structural parts, die life is dominated by the same eight failure modes, but the projected area, section changes, and deep cores push dies toward the lower end of the shot range unless cooling, intensification, and slide systems are engineered in from the quotation stage, as outlined in the 1,600–2,000T structural-part tonnage reference. Lead-time planning, which is now a multi-quarter constraint for new clamp force tiers, must therefore include die-rebuild slots in the production calendar, not just first-article dates, per the die casting machine lead time 2026 reference.
Standards, Sourcing, and Procurement Caveats
There is no single ISO or NADCA standard that prescribes a numeric die-life value for aluminum HPDC; the accepted practice is to define end of life contractually as the point at which the die can no longer produce parts that meet agreed dimensional, integrity, functional, or appearance requirements at an acceptable and stable production cost [S2]. A responsible quotation therefore states the assumed failure modes, the maintenance plan, the replaceable elements, and the commercial definition of end of life, rather than promising an unsupported shot count.
Procurement teams that treat die life as a fixed number usually end up either over-specifying (driving up tool steel and surface-treatment cost for life they will not use) or under-specifying (missing replaceable-insert features that would have protected the main die investment). For buyers weighing mold base steel sourcing, the alloy surcharge mechanics on mold base steel is now a material line item in any die-life cost model.
For shops with a mix of process technologies, a gravity die casting machine cell running the same alloy typically sees longer die life than a high-pressure cell on the same part, simply because injection energy and thermal shock are lower; the trade-off is cycle time and surface finish, not die life economics in isolation.
Limits of the Published Numbers and What to Track Next
Most public die-life ranges (50,000 to over 200,000 cycles for heavy equipment, 75,000 to 200,000 for general aluminum HPDC, and 100,000 as a common midpoint) come from OEM and supplier pages rather than from peer-reviewed studies, and the underlying assumptions on alloy, steel, geometry, and maintenance are usually compressed into a single sentence [S2][S3][S6]. Predictive models based on die surface temperature have been published for HPDC, but the data sets are small and process-specific, so the headline numbers should be treated as order-of-magnitude references, not as warranty values [S5][S9].
Two signals are worth tracking over the next two to four quarters: the uptake of condition-monitoring sensors (die-temperature mapping, cooling-flow telemetry, vacuum-integrity logging) on new aluminum die casting machines, and the publication of any revised NADCA or ISO/TC 306 guidance on die-life testing protocols. Either would tighten the range above and move die life from a quotation-line item to a measured, auditable process variable.