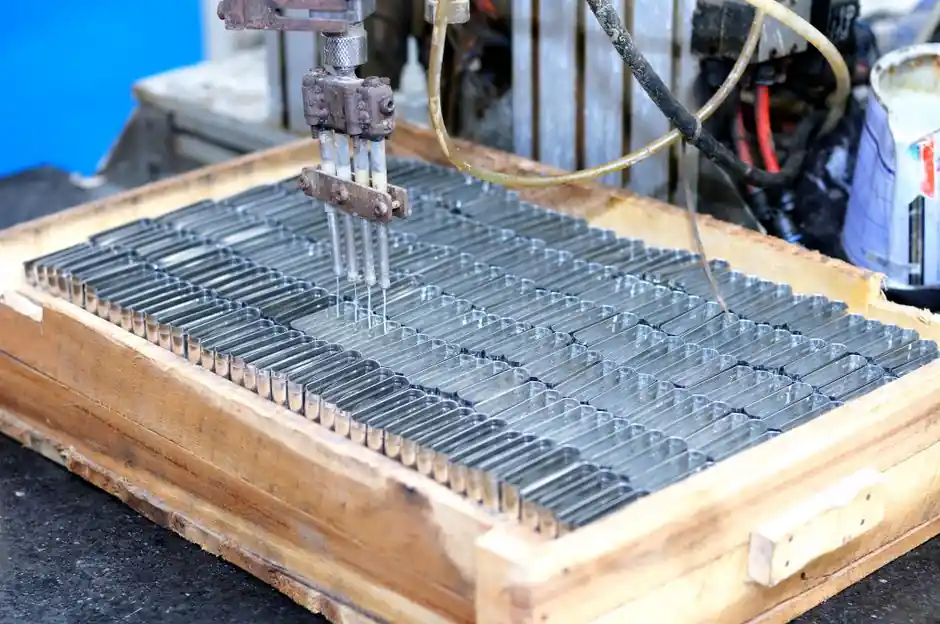
Die casting machine lead time in 2026 is governed by clamp force tier: prototype-class units in the 20-500 ton range deliver in 10-15 working days through modular soft-tooling workflows, while the 4,001-10,000 kN mid-band (roughly 400-1,000 metric tons) controls 53.08% of the global installed base, and machines above 10,000 kN (1,000+ tons) routinely run 32-52 week delivery cycles from purchase order [S1][S2].
The split exists because the 4,001-10,000 kN band corresponds to the mainstream automotive structural casting workhorse, and the 10,000+ kN band covers giga-press class equipment used for single-piece EV underbodies and battery tray castings. Process engineers sourcing a die casting machine in 2026 should treat clamp force as the primary lead-time driver before evaluating injection unit, platen size, or controls retrofit scope [S2][S6].
Small-Tier Lead Time: 20-500 ton Hot-Chamber and Bench Units
Zinc and lead hot-chamber machines in the 20-88 ton clamp range ship from catalog stock, with multi-slide models such as the Techmire 24NTX and 44LCX rated at 20-22 metric tons (roughly 200 kN) and built for dry-cycle rates up to 4,500 cycles per hour [S5]. These units are typically off-the-shelf with 4-8 week delivery for standard configurations, and 10-12 weeks when paired with custom multi-slide tooling or parting-line injection packages.
For the 80-500 ton band, which covers most prototype and short-run aluminum gravity die casting machine work plus small zinc HPDC, modular soft-tooling workflows deliver T1 sample parts in 10-15 working days, with full tolerance capability of ±0.02 mm on critical features and 40-60% cost reduction versus hardened H13 production tooling [S1]. Rapid tooling typically uses P20 or aluminum molds rated for 5,000-50,000 shots, and partners with 80T-2,500T capacity can transition prototype parts directly into production without retooling [S1].
Mid-Tier Lead Time: 500-4,000 kN (50-400 metric ton) Cold-Chamber Workhorses
The 500-4,000 kN band covers the bulk of Tier-1 automotive structural components, consumer electronics housings, and small appliance castings, and lead times here run 16-26 weeks from PO for new machines. Machines in this range are typically built to order, with delivery stretching to 30+ weeks when integrators add tie-barless platens, servo-hydraulic shot control, or integrated trim presses. [S2]
Shibaura Machine's DC series, introduced in 1961, standardized cold-chamber designs from 80 to 800 ton (roughly 800-8,000 kN) clamp force, establishing the engineering baseline still in use for this mid-tier today, with the 1966 DC*A series adding the pressure-buildup timing improvements that later evolved into the independent injection/pressure circuits of the DC*C line [S3]. The mid-tier lead time is sensitive to platen size and shot weight; a 1,500 kN machine with a 5-7 kg aluminum shot weight usually lands in the 20-24 week window when ordered through a regional integrator.
Dominant Mid-High Tier: 4,001-10,000 kN (400-1,000 ton) Holds 53% of Market
By casting-machine clamping force, 4,001-10,000 kN machines held 53.08% share of the die casting market in 2025, confirming this band as the volume sweet spot for automotive structural castings, transmission housings, and large aluminum aluminum die casting machine sub-assemblies [S2]. Lead times in this dominant band average 28-36 weeks for new builds, with the 8,000-10,000 kN ceiling often pushing to 40 weeks because of larger platen castings, tie-bar machining, and longer hydraulic accumulator fabrication cycles.
For an aluminum die casting machine in this clamp class, integrators usually require 10-14 weeks for engineering kickoff, FAT planning, and logistics scheduling before delivery. The high-pressure die casting segment overall reached USD $40.05 billion in 2025 and is forecast at $57.43 billion by 2031 (6.19% CAGR), with automotive accounting for 61.23% of demand and EV battery housings plus motor components expanding at 10.35% CAGR, which is 4 percentage points above the broader market, so the 4,001-10,000 kN tier is the one most exposed to multi-quarter backlogs [S1][S2].
Giga-Press Tier: Above 10,000 kN (1,000+ ton) Lead Times Hit 32-52 Weeks
The over-10,000 kN segment is forecast to grow at 9.61% CAGR through 2031, the fastest of any clamp-force band, and individual machine deliveries in this class regularly run 32-52 weeks from purchase order [S2]. These are the units behind the EV megacasting trend: IDRA Group, Bühler, and UBE class machines in the 6,000-9,000 ton (roughly 60,000-90,000 kN) range are not uncommon, and a 2,000-ton Bühler-class install at a North American caster illustrates the upper end of the commercial envelope [S7].
Lead time at this tier is driven less by clamp tonnage than by platen size, shot weight, and integrated cell scope: a 6,000+ ton giga-press cell with automatic die change, sprayer robotics, and extraction conveyors will routinely take 14-18 months from PO to first good part, with FAT, sea freight, and on-site rigging adding another 10-14 weeks on top of build time. The 53.08% concentration of the 4,001-10,000 kN band, combined with the 9.61% CAGR push in the over-10,000 kN segment, means specifiers should lock in slot reservations 12-15 months ahead of the production-ready date for any giga-class program [S2].
Selection Criteria: Match Clamp Force Tier to Part Geometry First
Clamp force requirement is calculated by multiplying the cumulative projected area of mold cavities plus the gate and runner system by the pressure of the metal melt, typically 30-80 MPa for aluminum HPDC and 15-25 MPa for zinc hot-chamber work [S6]. A practical first-pass budget is 60-80 MPa of specific pressure on the projected area for safety-critical structural castings, 40-60 MPa for cosmetic consumer parts, and 25-40 MPa for thin-wall consumer electronics.
Part size is the other hard gate: larger machines with greater clamp force require more die close and clamp time, which adds 1-3 seconds per cycle versus smaller-tonnage units, so over-spec'ing a 1,500 ton machine for a 300 mm part wastes both capital and cycle time [S4]. Tier choice should also reflect alloy and process: zinc hot-chamber units below 200 kN cover most connector and lock hardware, while a vacuum die casting machine above 5,000 kN is the right call for structural aluminum with porosity targets under 1%.
Criteria-Based Comparison: 4 Clamp-Force Tiers Against 4 Decision Variables
Four clamp-force tiers are lined up against four procurement decision variables, so specifiers can match the band to their program risk and cash-flow tolerance: [S1]
- 20-200 kN (2-20 ton, zinc/lead hot-chamber): lead time 4-12 weeks, capital cost low (under $150K for catalog units), suitable for connector/lock hardware and short-run zinc prototypes, not for structural aluminum [S5].
- 200-4,000 kN (20-400 ton, aluminum HPDC, prototype/mid-run): lead time 10-15 days on soft-tooled parts, 16-26 weeks on the machine, capital cost mid, fits 80-500 mm castings, not for single-piece EV underbodies [S1].
- 4,001-10,000 kN (400-1,000 ton, mid-high tier): lead time 28-36 weeks, capital cost high, holds 53.08% of market, covers the dominant automotive structural and EV battery housing work [S2].
- Above 10,000 kN (1,000+ ton, giga-press): lead time 32-52 weeks plus 10-14 weeks rigging, capital cost very high, the only band capable of 1.5-2.0 m single-piece underbody castings, growing 9.61% CAGR [S2][S7].
Who This Lead-Time Map Is For, and Who It Is Not For
The clamp-force tier map is built for process engineers and procurement leads at Tier-1 automotive suppliers, EV OEMs, consumer electronics casters, and contract manufacturers who are sizing a new machine order 12-18 months out from first good part. It is not a fit for buyers shopping catalog zinc hot-chamber units for sub-200 kN work, where the Techmire 24NTX or 44LCX class machines ship from stock in 4-8 weeks without tier-based planning [S5].
Foundries evaluating magnesium die casting machine additions for EV battery and motor housings also sit in the 4,001-10,000 kN band, where the 9.53% CAGR in magnesium raw-material demand through 2031 and the 10.35% CAGR in EV components will stretch 28-36 week lead times into the 40-week range by mid-2027 [S1][S2]. Buyers who need parts, not machines, should treat the 10-15 working day prototype lead time as the relevant number, and source through a partner with 80-2,500 ton capacity and IATF 16949 certification rather than specifying the machine themselves [S1].
Limitations, Failure Modes, and Sourcing Signals
Lead time estimates above assume standard configurations: tie-bar platen, conventional hydraulic shot, and IEC 60204-1 / ISO 9001 base controls. Non-standard scopes commonly add 8-16 weeks: tie-barless platen, servo-hydraulic injection, integrated vacuum package (raising system cost 15-25% but cutting porosity 50-70%), automatic die change, and robotic sprayer/extraction cells. [S5]
Failure modes in the longer lead-time bands include platen casting porosity discovered at FAT (delays 6-10 weeks), hydraulic accumulator sourcing from a single qualified supplier, and integrator queue depth that varies 4-12 weeks by region. Two trackable signals for 2026 sourcing: the 4,001-10,000 kN share reading in next year's Mordor Intelligence update (expected to drift up as EV content-per-vehicle rises), and the percentage of the 10,000+ kN band that is booked into 2027 delivery slots, which the 9.61% CAGR implies is already the constraint [S2]. On the alloy side, non-heat-treated structural die casting alloy choice directly changes the required specific pressure, which feeds back into the clamp force selection above.