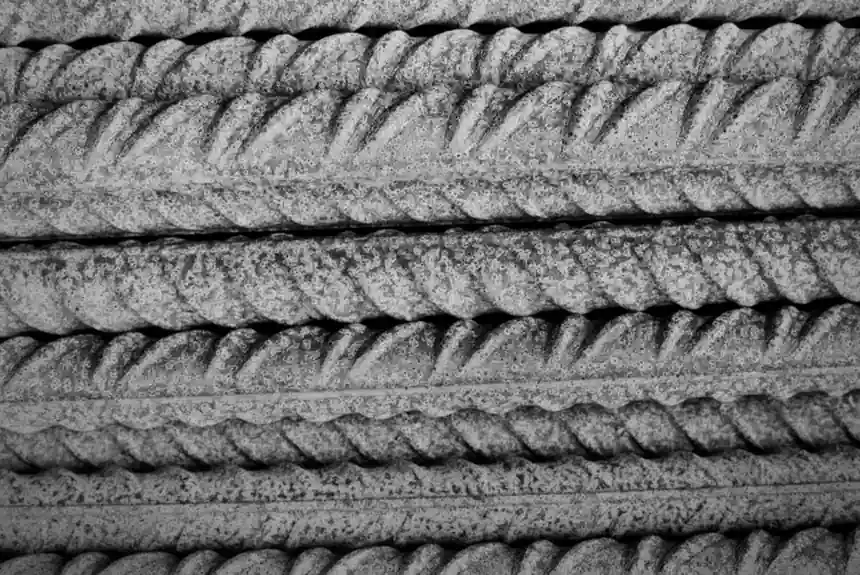
Both B500B and B500C rebar are defined under EN 10080 with the same characteristic yield strength of 500 MPa, so the structural capacity is identical on paper; the selection driver is ductility class, not strength [S3][S4][S6].
The practical split is straightforward: B500B is the default ductility class for bars, cages, and most structural members, while B500C is reserved for high-seismic detailing, dynamic loading, and members where post-yield deformation capacity must be demonstrated to the engineer of record [S2][S5]. Buyers should know that B500C typically carries a cost premium, and is rarely required where B500B can be substituted [S3][S4].
Standards and grade families
EN 10080 is the parent specification for weldable reinforcing steel and is adopted as BS 4449 in the UK, with national mirror standards across the EU [S2][S6]. The 500 in the grade name is the characteristic yield in MPa; the letter A, B, or C is the ductility class, ordered from lowest to highest elongation capacity [S3][S4]. B500A is generally restricted to spot-welded mesh, B500B is the workhorse for cut-and-bent bars and cages, and B500C is the seismic-grade option [S3][S4][S7]. A complete reference for stock form, diameters, and chemistry is maintained on our rebar encyclopedia entry.
Mechanical properties side by side
The single most useful comparison is the ductility block, because yield strength is held constant across the three classes at Re = 500 MPa with Re,actual / Re,nominal ≤ 1.25 [S3][S4]. B500B sets minimum total elongation at ultimate tensile force Agt ≥ 5.0% and a tensile-to-yield ratio Rm/Re ≥ 1.05; B500C raises both bars to Agt ≥ 7.5% and Rm/Re ≥ 1.15 (capped below 1.35) [S3][S4]. For fatigue, both B500B and B500C are rated at 2σa = 175 MPa for bar diameters d ≤ 28 mm, dropping to 145 MPa for d > 28 mm, versus a flat 100 MPa for B500A spot-welded mesh [S1][S3][S4].
Chemistry, weldability, and processing
EN 10080 governs mechanical performance and weldability rather than locking a tight composition window, so producers tune C, Mn, Si, P, and S to hit the ductility class while keeping carbon equivalent Ceq ≤ 0.50 [S3][S4][S5]. A typical published maximum for B500B is C ≤ 0.22%, Mn ≤ 1.5%, Si ≤ 0.55%, P ≤ 0.05%, S ≤ 0.05% [S2]. Because the carbon equivalent ceiling is the same for both grades, weldability with standard low-hydrogen electrodes is effectively equivalent; the difference shows up at the bend-and-rebend test and during prefabrication, where B500C absorbs more cold deformation before surface cracking [S2][S5].
For shop fabrication, B500C is friendlier on tight-radius stirrups, hooked bars, and seismic hoops, because the higher Agt reserve lets the steel survive cold bending without micro-cracking the ribs; B500B is fully adequate for routine straight bars, standard links, and 180° bend tests at the supplier-published mandrel sizes [S2][S5].
Stock form, diameter range, and tolerances
Diameter availability is identical between the two grades at 6–50 mm for the nominal centreline, supplied as coil, straight bar, or as part of spot-welded mesh and lattice girders, and tolerance on the nominal centreline is held to ±4.5% on both [S3][S4]. B500A is the outlier here, limited to 4–16 mm because it is used almost exclusively in mesh products [S3][S4]. In real procurement, that means B500B and B500C are interchangeable on the rebar shelf, and the substitution question collapses to ductility and price, not to whether the bar can be sourced in 12 mm or 32 mm.
Where B500B is the right call
For residential frames, commercial slabs, foundations, retaining walls, bridges without seismic detailing requirements, and most industrial structures, B500B is the default because it clears every EN 10080 and BS 4449 mechanical check at the lowest mill price [S2][S6]. Hot-rolled ribbed B500B is normally produced in 8–40 mm diameters, in 6 m or 12 m straight lengths, or in coil form at ≤ 16 mm, with bundles tagged to heat number for full traceability [S2]. Where pre-cut and pre-bent cages are specified, the rebar bender workflow assumes a B-class ductility reserve for hook recovery.
Where B500C is genuinely required
High-seismic zones (Eurocode 2 ductility class DC "H" or DC "M" frames in regions of high design ground acceleration), critical infrastructure such as nuclear and LNG structures, members designed for plastic hinge rotation, and projects where the specification explicitly calls out EN 1992-1-1 Class C ductility are the cases where B500C is non-substitutable [S2][S5]. The same Rm/Re ≥ 1.15 ratio and Agt ≥ 7.5% elongation are what allow the structural designer to claim ductility class C in the reinforcement schedule without performing additional qualification testing [S3][S4][S6].
Cost, sourcing, and market signals
Multiple stockists note that B500C "usually has a significant cost overhead" and is "rarely required" where B500B satisfies the design, so procurement should default to B500B and only step up to B500C when the EOR has flagged seismic or high-ductility detailing on the drawing [S3][S4][S7]. International reference pricing for B500B in 2025 has been reported in the USD 520–600 per MT FOB band, with surface treatment (epoxy, galvanizing) and mill origin driving the spread [S2]. A wider look at mill-side dynamics, including EAF-share growth and scrap-quality trends that shape the next decade of rebar supply, is in the EAF share growth and scrap quality trends analysis.
Selection checklist before you sign the PO
Confirm the ductility class on the structural drawing (B or C) and the member type it applies to; confirm whether fatigue at 2σa = 175 MPa for d ≤ 28 mm is required, which both B500B and B500C meet, versus 100 MPa for spot-welded mesh where B500A is the only fit [S1][S3][S4]. Specify the bar surface (plain ribbed for B500B/B500C, ribbed or smooth for B500A), the diameter range, and whether the bars will be cut-and-bent on a rebar bender for pre-assembled cages. Finally, require EN 10080 / BS 4449 mill certificates with heat-number traceability and third-party inspection for any seismic-zone or export shipment, and you will avoid almost every dispute seen on cross-grade substitutions [S2][S6].
Trackable signals for the next sourcing cycle: published mill price moves in the USD/MT FOB range for B500B out of Turkey and the UAE, and any tightening of Ceq limits in future EN 10080 amendments that would change the B500B/B500C weldability assumption. For context on how reinforcement steel demand tracks with adjacent construction inputs, the PN16 vs PN25 PPR pipe pricing breakdown covers a comparable material-substitution decision on a different building system.
Spec-level background on the components involved: checking and testing apparatus.