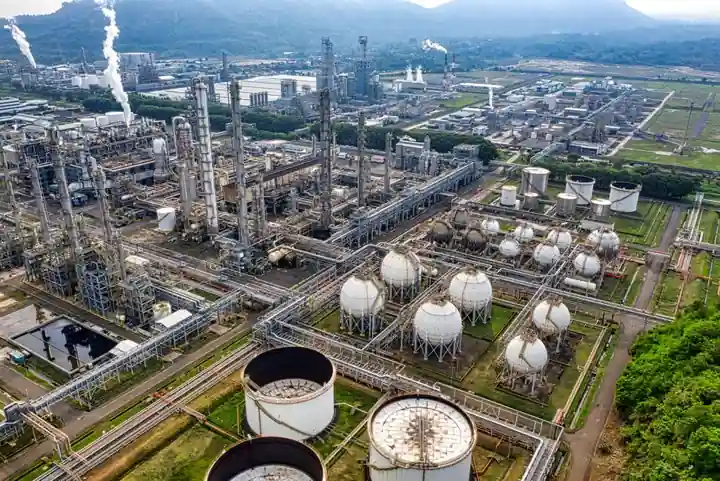
High-pressure gas ball valves for transmission and process service are commonly rated from 275 PSI (Class 150, 100 °F) up to 1,000 bar (15,000 psi) at 752 °F (400 °C), with body sizes spanning 0.2 to 48 inches [S1][S9].
The datasheet is the only document a process engineer sees before signing off on a valve, so every line item (pressure-temperature class, body style, seat material, port configuration, fire-safe certification, test pressure) must match the line condition, otherwise the wrong valve goes into a combustible-gas line and the consequence is rarely a small one [S2][S3].
Pressure-Temperature Class: the Single Most Important Datasheet Line
ASME B16.34 defines the pressure-temperature class system, and a Class 150 stainless steel ball valve is rated 275 PSI (19.0 bar) at 100 °F but derates to 200 PSI (13.8 bar) at 400 °F [S3][S9].
Natural-gas service spans 1/4 PSI residential up to 1,500 PSI on large transmission lines, so a single class does not fit the whole network: Class 150 dominates boilers and commercial buildings under 5 PSI, Class 300 covers mid-range distribution, and Class 600, 900, 1500, and 2500 cover compressor stations and high-pressure process headers [S3]. A “600 WOG” marking, meaning water, oil, or gas, is a body-pressure rating of 600 PSI independent of ASME class and must not be confused with the temperature-derated ASME Class 600 figure [S8].
Floating vs Trunnion-Mounted: a Size-and-Pressure Decision
Floating-ball designs rely on line pressure to push the ball against the downstream seat, which means operating torque rises with pressure and the geometry is normally limited to small sizes, while trunnion-mounted designs fix the ball on top and bottom stems and are the standard for valves larger than 8 inches or above Class 600 [S2].
For high-pressure gas, trunnion is almost always the correct call: the fixed pivot decouples operating torque from line pressure, the seats are bidirectional, and the body can be specified as fully welded for buried or subsea service where external leak paths are unacceptable [S1][S2]. A welded body removes the side-entry bolted flange as a leak path, which matters for any gas line that will never see a shutdown for maintenance.
Body, Seat, and Stem Materials on the Datasheet
Common gas-service body materials are brass, cast iron, and stainless steel, with stainless selected when the line pressure and corrosion exposure rule out the cheaper alloys [S3][S10].
Seat material follows the application: PTFE soft seats give the tightest shutoff for clean, dry natural gas at moderate temperatures, while metal seats (stainless or tool steel) are required for high-temperature gas, abrasive service, or any line where a fire can destroy a polymer seat [S3]. Stem seals are typically PTFE or another high-performance polymer; a leaking stem is just as dangerous as a leaking seat on a combustible-gas line [S3]. For high-pressure rated units, floating balls are often chrome-plated to extend service life under repeated seat contact [S1].
Port, Bore, and Flow Coefficient (Cv)
Ball valves are specified as full port (bore equal to the pipe ID) or reduced/regular port; full port minimizes pressure drop and is preferred for gas service where any avoidable ΔP wastes compressor energy [S2].
The Cv value published on the datasheet is the flow coefficient at a defined travel, and combined with line pressure and gas specific gravity it gives the engineer a real flow rate rather than a nominal “DN50” guess [S3]. A useful quick sanity check: a 600 WOG body and a published Cv together tell you whether the valve can pass the design SCFM without choking, before you commit to a purchase order [S8].
Fire-Safe and Combustible-Gas Certifications
For flammable-gas service the datasheet must show API 607 (fire-safe for quarter-turn valves) and, for North American gas distribution, CSA 3.16-15, which covers metallic lever-operated gas shut-off valves with flanged, threaded, or welded ends, service temperatures from -76 °F (-60 °C) to 356 °F (180 °C), and a 125 PSI upper limit [S3][S4].
CSA-rated valves are sub-classified: the BRS125G / CAN 3.16 marking is the outdoor rating, while indoor valves carry 1/2 PSI (appliance-mounted) or 5G (household piping) markings at lower test pressures [S4]. On pressure-regulating and isolation stations, paired safety-relief valves and pressure-reducing valves downstream of the ball block must be selected against the same ASME class, otherwise the block valve is the strongest link in a chain the rest cannot hold. For an electric-actuated isolation valve, the electric ball valve datasheet adds actuator torque, voltage, and enclosure rating (often NEMA 4 or 4X) to the same body spec.
Body Style and End Connections
Five body configurations show up on industrial datasheets: one-piece, three-piece, split-body, top-entry, and fully welded; one-piece is the cheapest and disposable, three-piece allows seat and seal replacement without cutting the valve out of line, and fully welded is the buried-service default [S1].
End connections are typically flanged (ASME B16.5), threaded (NPT), butt-weld, or press-fit systems such as the Apollo PowerPress® range, which is rated for thick-wall steel pipe per ASTM A53, A106, A135, and A795, Schedule 10 to 40 [S7]. For larger diameters the 8-inch floating/trunnion crossover is the right place to revisit the datasheet, because trunnion becomes the engineering default above that size [S2].
Hydrostatic and Pneumatic Test Pressures
Standard hydrostatic shell test pressure is 1.5 times the cold working pressure rating, and the seat test is typically 1.1 times the valve pressure rating, with the exact multiplier depending on the certification scheme called out on the datasheet [S2].
Every datasheet should be checked against the line’s maximum allowable working pressure (MAWP) at design temperature, with a 10 to 25 percent engineering margin, and CSA 3.16-15 valves are acceptance-tested at 125 PSI for outdoor service before shipment [S2][S4]. Skipping that cross-check is the single most common cause of a brand-new valve being non-compliant the day it arrives on site, and the fix is to compare the published shell test number to the line MAWP before the PO is cut [S6].
Datasheet Comparison: Main Options for High-Pressure Gas
Two-way ball valves for high-pressure gas split into four practical choices that line up against the datasheet axes: (1) Floating-ball, PTFE seat, Class 150/300, brass or stainless body suits residential-to-light-commercial dry gas up to ~300 PSI; (2) Trunnion-mounted, PTFE seat, Class 600, stainless body suits midstream distribution and metering skids; (3) Trunnion-mounted, metal seat, Class 600 to 2500, alloy body suits high-pressure gas with elevated temperature or sour service; (4) Fully welded trunnion, Class 600 to 1500, stainless body suits buried or subsea transmission where external leak paths cannot be tolerated [S1][S2][S3].
The first option is wrong above 600 PSI or 8 inches because the seat load and operating torque climb beyond what a floating geometry can handle, while the last two are over-spec for indoor appliance lines and waste capital on metallurgy the application does not need [S2][S3]. Specifying a high-voltage tester for the actuator circuit on electric-actuated isolation valves, or sourcing ball bearings for valve trunnion service, follows the same datasheet discipline: the published rating only counts if the line condition sits inside the published envelope.
Maintenance and Operating Signals Worth Tracking
Verify the datasheet pressure rating against the system MAWP at every maintenance interval, and replace seats and seals at the manufacturer-published cycle count rather than on failure, because a worn seat on a gas block valve rarely gives a visible leak before it fails [S6].
Track on the datasheet: number of cycles, peak torque recorded at the actuator, and any temperature excursions outside the published seat envelope; these three data points predict end-of-life within one overhaul cycle and are the signals to watch through 2026 as more operators move from calendar-based to condition-based valve maintenance on gas-service assets. For a related view on adjacent isolation hardware, the ball retainer vs full complement discussion covers how retainer geometry changes load capacity in a similar datasheet-driven selection, and the API 610 vs ASME B73.1 piece shows the same pressure-class logic applied to pumps paired with these block valves.