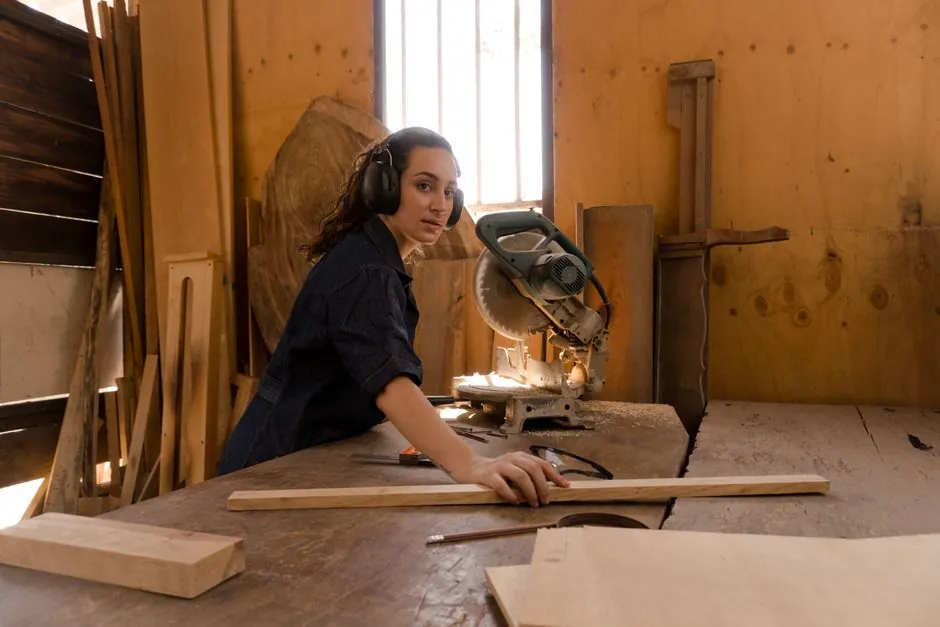
For aluminum gate cutting on circular saws, TCT (tungsten carbide-tipped) blades are the dominant specification, with multiple sources naming them the most popular and widely recommended option for non-ferrous metal work [S1][S2][S3].
HSS (high-speed steel) blades remain in use, but only as a lower-cost, lower-durability alternative suited to thin sheets, light-duty cuts, and occasional production [S1][S2]. The decision turns on tooth material hardness, allowable cutting speed, blade life, and the surface finish the gate fabricator needs.
Tooth Material and Heat Behaviour: Why Carbide Runs Hotter and Faster
TCT blades are built from an alloy-steel body with tungsten carbide tips brazed onto each tooth, and carbide's hardness and heat resistance let the blade run at a higher RPM than HSS while keeping an edge [S2][S4].
HSS cold-saw blades are machined entirely from high-speed steel, with a variable tooth pitch that limits vibration and aids chip evacuation; TiN and TiAlN coatings are commonly used to stretch their service life [S4]. The trade-off is that HSS loses temper when overheated: experienced operators watch the chip colour and treat a straw hue as the safe limit, with blue indicating the steel has started to give up hardness [S7].
For aluminum gate profiles, this heat gap matters because aluminum conducts heat away from the cut and can weld swarf to the teeth if friction runs away; a tooth material that stays hard at higher temperature is a direct mitigation [S1][S4].
Cutting Speed, Wear Life, and Productivity on Aluminum
Compared with HSS, carbide is significantly harder and can maintain cutting performance at higher cutting speeds, which translates directly into higher productivity on long production runs of gate extrusions and plate [S2].
HSS blades are credited with good toughness, good resistance to impact, and the ability to be resharpened several times, which keeps their per-blade cost down for low-volume or intermittent cutting [S2]. The catch is shorter blade life and faster dulling, and once an HSS saw goes blue, the body is softened and the edge is gone [S2][S7].
PCD (polycrystalline diamond) blades sit at the top of the aluminium-cutting pyramid, with exceptional longevity and superior edge quality on industrial production lines, but the upfront cost rules them out for typical gate-fabrication volumes [S1].
Tooth Count and Geometry for Clean Gate Cuts
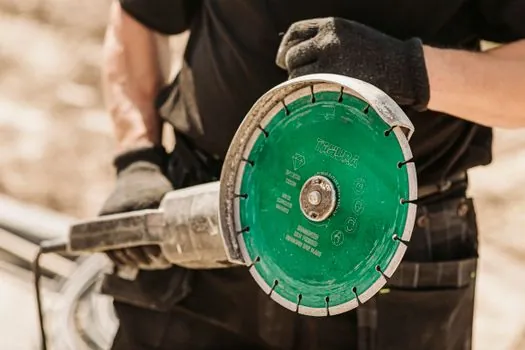
Tooth count is a primary lever for cut quality on aluminum, and 80-120 teeth on a 10-inch blade is the published band for thin aluminum sheet, 60-80 teeth for thick plate, and 80-100 teeth for extrusions and profiles [S1].
Triple-chip grind (TCG), an alternating flat-top and trapezoidal tooth pattern, is the most recommended tooth design for aluminum and is what most "non-ferrous" labeled blades carry [S1][S5]. Practical shop-floor guidance is to use a 10-inch 60-tooth blade on a table saw, or a 12-inch 80-tooth TCG blade on a chop saw, with stick wax or tallow applied to the teeth as a lubricant [S5].
Higher tooth counts cut slower but produce smoother finishes with less burr, and most professional gate work values finish over raw feed rate, so overspec'ing teeth is the common choice [S1].
Decision Matrix: HSS vs TCT for Aluminum Gate Work
For gate shops choosing between an HSS and a TCT circular saw blade, the four criteria that matter are cutting speed, wear resistance, blade life, and resharpening economics. HSS is rated moderate on speed and good on wear and toughness, with the advantage of multiple resharpenings at a lower upfront price [S2]. TCT is rated higher on speed, excellent on wear, and longer on life, with a higher initial cost that gets paid back on volume [S2][S4].
For gate profiles, structural extrusions, and plate that get cut daily, TCT is the correct default; for one-off gate brackets, thin trim pieces, or a shop that already has HSS resharpening in house, HSS still earns its place. A cutting machine paired with a TCG TCT blade is the standard configuration cited across cold-saw and miter-saw guidance for aluminum extrusions [S1][S4].
The third axis is tolerance for chip welding and burring: aluminum's tendency to stick to teeth makes anti-stick blade geometry and a lubricant (stick wax, tallow, or in some shops WD-40) more than a nicety, they are part of the spec [S1][S5].
Failure Modes and Shop-Floor Signals
The first signal a blade is failing on aluminum is edge quality: increasing burr, vibration, and rough cuts all point to a dulled or chipped tooth before the blade actually stops cutting [S1].
On HSS, the warning is colour: a straw temper colour is the practical limit, and any blue tint on the tooth body means the steel has exceeded its tempering temperature and lost hardness [S7]. On TCT, the warning is chipping of the carbide insert rather than softening, since carbide stays hard but is more brittle than HSS and hates impact loading and contamination [S2][S4].
For gate work, the practical mitigation is matched blade and machine: a high-RPM miter or table saw with a TCG TCT blade and wax lube for daily cutting, with HSS reserved for back-up or thin-stock work where its lower cost and resharpenability offset the speed penalty [S1][S2][S5].
Standards, Lubrication, and Shop Practice
There is no single ASTM or ISO rule that picks the blade for you; selection is driven by tooth material (carbide vs HSS), tooth geometry (TCG for non-ferrous), and tooth count matched to wall thickness, with stick wax or tallow as the near-universal shop lubricant for both blade types on aluminum [S1][S5].
Cold-saw guidance is consistent that carbide-tipped blades rotate at higher speeds than HSS because of carbide's heat resistance, and that carbide tips are precisely ground to defined cutting angles rather than rely on coatings [S4]. For high-volume gate production this is the productivity argument that drives the TCT default; for prototype or one-off gates, a quality carbide-tipped wood blade on a miter saw is a documented field solution, with stick wax as the only additive [S5].
Trackable next signals for specifiers: the 10-inch 60-tooth TCG TCT blade and 12-inch 80-tooth TCG TCT blade remain the published baseline sizes for table-saw and chop-saw gate work, and PCD-tipped blades are the credible upgrade path when cut counts per shift push past the economic life of TCT [S1][S5].
Spec-level background on the components involved: silicon carbide.
Background reading: Edge vs Cloud Analytics for Vibration Data: 2026 Deployment Matrix.