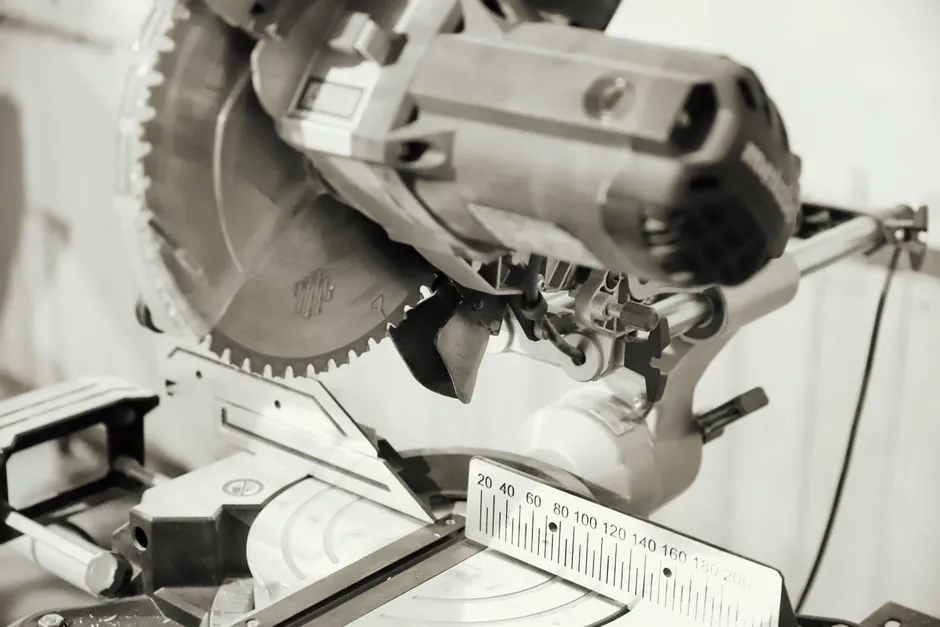
Choose a horizontal bandsaw for repeated square-tube production because it cuts cleanly with low chip volume and little edge finishing, while a portable cold cut-off saw suits short runs and limited space [S1][S3].
The comparison depends on cut quantity, tube wall, required squareness, blade economics, and tolerance for chips, noise, heat, and downstream deburring, rather than on the generic term “chop saw” [S1][S4].
Separate abrasive cut-off saws from metal-bladed cold saws
An abrasive chop saw is extremely loud, produces dirty cuts, and may leave a burr that requires grinding. A horizontal band saw produces a clean cut with no dust, though one respondent said it is slower than a chop saw.
A carbide dry cut-off saw reportedly cut steel square tube effectively, although it produced a substantial mess of shavings.
For a fabrication shop, the cited respondent recommended a horizontal band saw because it improved cut quality, reduced fabrication time, and eliminated the need to grind large burrs from every cut. The related guide on cold saw blade tooth count for steel versus aluminum is useful after the machine decision because tooth selection must match the material and section.
Compare speed, finish, chips, and operating cost
Bandsaws are generally slower than chop saws, but they produce cleaner cuts, less abrasive dust, and parts that require less grinding or sanding. Their lower chip volume is a direct consequence of the cutting action: each tooth removes a discrete chip instead of an abrasive wheel pulverizing a wider kerf into debris [S1][S3].
A cut-off saw is better suited to rapid stop-and-start work where the operator brings the descending blade to each marked length.
Blade economics favor the bandsaw in production. Band saws use thinner blades than cold saws, while one dry cold-saw report records about 250 cuts from a factory carbide blade and replacement blades priced around US$80–140. The same report lists portable band-saw blades at approximately US$10–20 [S5]. These are field observations rather than universal prices, but they explain why blade cost can dominate low-volume versus high-volume economics.
Use a bandsaw when square tube is the recurring feedstock
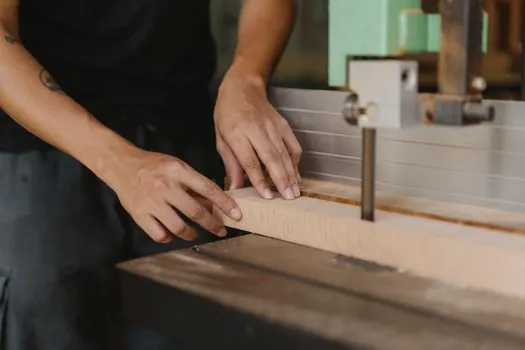
For fabrication-shop production, the cited respondent recommended a horizontal band saw because it provided better cut quality and reduced the need for grinding. A horizontal band saw can reduce the need to remove a large burr from every cut.
Tube geometry makes tooth selection less straightforward than for solid bar.
Blade pitch must therefore match wall thickness and material rather than tube width alone. The cited guidance identifies 24 TPI as a fine-blade example for cutting 1-inch material and says that too few teeth relative to workpiece thickness can break teeth and produce a rough cut.
Use a cut-off saw for portable and occasional fabrication
A cold cut-off saw is the better fit for a small shop, field fabrication, or an irregular flow of short tube cuts. One respondent chose a band saw partly because space was a major factor.
The limits become clear in repeated production. A shop using a 14-inch abrasive chop saw for tube up to 4 inches by 1/4-inch wall reported about one blade per year and worsening angular cut quality as tube size and wall thickness increased. Moving to horizontal band saws improved cut quality, reduced fabrication time previously spent grinding off burrs, and eliminated the persistent grinding smell [S4].
A carbide dry cut-off saw does not heat the parts much, but it produces a substantial mess of shavings that is difficult to clean. A cut-off machine comparison should also include the requirement for accurate square ends, not just cutting speed.
Select the machine from workload and acceptance criteria
Choose a horizontal band saw when monthly volume is repeated or production-like, square ends are the main quality requirement, and cleanup or downstream grinding must be minimized. Choose a cold cut-off saw when cuts are occasional, portability and rapid length changes matter, and the tube size remains within the saw and blade rating [S1][S4].
Use an abrasive cut-off saw only when low initial cost and rapid cutting outweigh dust, heat, noise, and finishing requirements. A stand-up portable band saw may also be too restrictive in throat depth for larger square tube, while a horizontal band saw is more suitable once the workpiece must pass fully through the machine [S2].
For mixed shops, the practical allocation is simple: reserve the cut-off saw for setup, repair, and one-off cuts, then reserve the horizontal band saw for production stock. A well-equipped fabrication shop can justify both because they solve different workflow problems rather than competing as identical substitutes [S1].
Validate the trial before committing to fleet capacity
Before purchase, cut representative tube in the actual material, wall thickness, and required length. Check end squareness with a square, measure burr formation, confirm blade speed and feed suit the section, and record time from marked length to separated part including cleanup [S1][S3].
Track two operational signals: cuts per blade and rework time per cut. A cold saw that cuts quickly but needs repeated deburring can lose its advantage, while a bandsaw that avoids grinding can justify a slower cycle [S1][S4]. Record coolant condition, chip volume, and blade replacement intervals as the three most useful indicators for deciding whether the machine matches the shop’s real workflow.