On a moving conveyor or assembly line, a fixed-mount scanner reads codes hands-free as parts pass a stationary read point, which is why it is the default form factor for high-throughput lines [S1][S3]. A handheld scanner, in contrast, requires a worker to aim and trigger each read, and its throughput is capped by the operator, not the line [S2].
The split between the two is a workflow decision, not a technology preference: if items move past a fixed point at known speed and orientation, choose fixed-mount; if a worker must go to the part, or the part arrives in unpredictable orientation, choose handheld [S2][S4]. For a deeper look at the wider scanner category, the industrial barcode scanner encyclopedia entry covers the technology families that both form factors draw from.
Where fixed-mount wins: throughput, repeatability, hands-free reads
Fixed-mount scanners are anchored to a conveyor frame, chute, workstation, or robotic arm, and they read codes as items pass by at line speed, with no operator in the loop [S1][S6]. On a production line, that means a single fixed unit can verify part IDs, batch numbers, and serial codes continuously, instead of tying up a worker per station [S3].
Decision-grade criteria for picking fixed-mount on a line: (1) item presentation is consistent (known distance, angle, and trigger), (2) read rate must match the conveyor or index time of the upstream process, (3) read point is unattended, (4) the code is fixed on the package or the part, not on a face the operator must rotate into view. Where all four hold, fixed-mount typically beats handheld on cost-per-read, because labour at the read point is removed entirely [S2][S3].
Fixed units also dominate where direct part marking (DPM) is used. Laser-etched or dot-peened codes on metal, plastic, and electronic substrates are common in automotive, medical device, aerospace, and defence lines, and fixed-mount readers are specified to handle them at line speed rather than relying on a worker to align the device [S5]. For the wider question of how these readers sit inside a line, the conveyor sorting line encyclopedia entry covers the upstream and downstream equipment that the scanner has to integrate with.
Where handheld wins: mobility, irregular presentation, short runs
Handheld scanners, both corded and cordless, put the reader in the worker's hand, which is the right answer whenever the part does not reliably come to a fixed read point [S2][S4]. Typical line-side cases are operator inspection of a held sub-assembly, repair and rework stations, short-run or changeover work where fixtures keep changing, and any point where the code is on a face that needs to be rotated into view.
Cordless handheld units configured for warehouse and line-side use transmit data over distances long enough to support fork-truck mounting and high-rack material handling, which keeps them useful as bridge devices between fixed and mobile workflows [S2]. For shop-floor traceability, they are also the practical choice when a code fails the fixed read and an operator has to re-scan the suspect unit before it leaves the cell.
One blunt sizing rule from integrators: if a human is always present at the read point anyway, a handheld is the natural choice, because adding a fixed mount to a station that already has an operator doubles the hardware cost without removing labour [S4]. A practical read on a molding line context makes the trade-off obvious: an injection cell where a moulded part is ejected and inspected by the operator is a handheld job, whereas a downstream cosmetic-inspection or pack-out conveyor after the cell is a fixed-mount job.
Comparison matrix: fixed-mount vs handheld on a line
The four criteria that actually drive the call are read-point attendance, item presentation, throughput, and total cost of ownership. Lining them up makes the decision mechanical rather than a brand debate. [S2]
Read-point attendance: fixed-mount is unattended (no operator required to trigger a read) [S1][S2]; handheld requires an operator to aim and trigger [S2][S4]. Item presentation: fixed-mount needs consistent distance, angle, and orientation of the code as it passes the reader [S3][S6]; handheld tolerates irregular presentation, multiple faces, and short-run changeover [S2][S4]. Throughput: fixed-mount is bounded by the line, not the operator, and is the form factor specified for DPM codes on automotive, medical, aerospace, and defence parts [S5]; handheld is bounded by the operator's aim-and-trigger cycle [S2][S3]. Cost-of-ownership logic: fixed-mount removes a scanning worker per read point in high-volume runs [S2]; handheld keeps capex lower and absorbs the operator's time, which is acceptable where an operator is already required at the station [S3][S4].
For an automated high-volume assembly or pack-out line, the matrix points to fixed-mount. For a workbench inspection, a repair station, or a low-volume kitting bench, it points to handheld. Most lines end up with both: fixed-mount at the unattended transfer and sortation steps, and handheld at the attended inspection and exception steps. When a line is being built new, the automatic molding line reference is a useful sanity check on where human attendance disappears entirely and fixed-mount reads become mandatory.
Selection criteria for fixed-mount on a new line
Four parameters drive the fixed-mount spec: symbology, sensing technology, read distance and field of view, and environmental rating [S3][S5]. Symbology: 1D (UPC, EAN, Code 128) is enough for case and shipper labels; 2D (Data Matrix, QR) and DPM codes need an imager-based reader with DPM decoding firmware, and this is the standard configuration in automotive, medical device, and electronics lines [S3][S5].
Sensing technology: laser-based fixed readers are still common for high-speed 1D reads on conveyor sortation, but area-imaging cameras have largely taken over for 2D and DPM, because a single imager handles multiple symbologies and tolerates more variation in part orientation [S2][S5]. Read distance and field of view must be matched to the conveyor width and the smallest X-dimension the line is expected to print or mark; under-specifying either is the most common cause of fixed-mount misreads in the field [S3].
Environmental rating: washdown, dust, and ambient-light conditions all push the spec toward an IP65-sealed fixed-mount module, and many line builders now specify IP65 by default for food, beverage, and pharmaceutical lines [S4]. Integration method matters too: fixed-mount units commonly expose USB, RS-232, and Ethernet, and the choice is driven by what the line PLC or line-side line-frequency furnace controls upstream can ingest without a protocol converter in the panel.
Selection criteria for handheld on a line
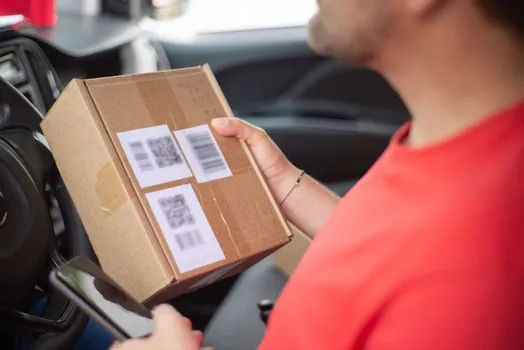
Handheld selection on a line is driven by three things: ruggedness, scan engine, and connectivity [S2][S4]. Ruggedness is rated by drop spec and sealing; industrial-grade handhelds are typically rated for multiple 2 m drops to concrete and IP65 sealing, which is the right baseline for shop-floor use where drops are routine [S2].
Scan engine: area-imaging engines read both 1D and 2D and tolerate damaged or poorly printed labels, which is the practical choice for a general-purpose shop-floor handheld; laser line scanners are cheaper but limited to 1D and clean labels [S5]. Connectivity: corded (USB, RS-232) is the right call at a fixed station where the operator never leaves; cordless (Bluetooth or proprietary 2.4 GHz) is mandatory when the operator walks the part to the reader or reads on a fork truck [S2].
One spec point that matters and is often missed: an industrial handheld configured for warehouse and line-side use can read at extended range, in the multi-metre class, which is useful at receiving docks and rack ends, but a short-range focused engine is the right pick for bench-top inspection where the operator is within arm's length [S2]. For mixed fixed-mount and handheld fleets on the same line, standardising on a 2D imager engine across both form factors reduces training cost and the spare-pool complexity.
Failure modes and integration constraints
Fixed-mount failures are almost always integration failures, not hardware failures. The most common are: trigger timing wrong for the line speed (read happens before or after the code is in the field of view), depth of field miscalculated for the smallest code on the line, and ambient light or strobe lighting from a vision system overpowering the imager [S3][S6]. Mounting on a robotic arm adds a second class of failure: cable management and IP rating of the arm-mounted unit, because the cable flexes every cycle [S3].
Handheld failures are different: trigger fatigue, missed reads on damaged labels, and cordless drop-off when the operator walks out of range [S2]. A common integration trap is specifying a consumer-grade handheld for shop-floor use; the unit works on day one and dies in the first quarter from drops, dust, or solvent exposure [S4].
Across both form factors, the underlying AIDC system contract is the same: the scanner is the physical interface between the real world and the MES or WMS, and a wrong choice does not mean the device fails to read, it means the workflow gets slower, less consistent, or more labour-intensive than it should be [S2]. That framing is why integrators treat the decision as a workflow design problem before it is a hardware problem.
Sourcing and standards to anchor the spec
Two standards-level anchors are worth keeping in the spec text even though they are not product-specific. ISO/IEC 15416 and ISO/IEC 15415 define the print-quality verification methods for 1D and 2D barcodes respectively, and they are the right references when a fixed-mount read-rate problem is traced back to marginal marking rather than the scanner. For DPM codes on metal and plastic, ISO/IEC 29158 is the dedicated direct-part-mark quality verification standard, and it should appear in the print-quality clause of any automotive or aerospace line spec. [S5]
On the device side, vendor datasheets are the practical reference for the read distance, field of view, minimum X-dimension, and IP rating of a specific fixed-mount or handheld model; integrators size the reader to the smallest code and the worst-case presentation on the line, not to the nominal case [S3][S5]. Two trackable signals to watch on the next spec cycle: (1) area-imaging engines continuing to displace laser engines in fixed-mount form factors for 2D and DPM work, and (2) cordless handhelds standardising on Bluetooth rather than proprietary 2.4 GHz radios, which simplifies spare-pool management on mixed-vendor lines [S2][S5]. A useful adjacent reference is the broader fixed gas detector encyclopedia entry, which follows the same unattended-read-point logic when a line needs continuous monitoring rather than periodic scanning.
This topic is covered further in Front vs Rear Discharge Concrete Mixer Trucks: Spec-Driven Selection.