A staged hot chamber commissioning sequence covers dry-cycle verification, hydraulic pressure ramp, gooseneck/nozzle preheat, alloy-temperature stabilization, shot-weight calibration, and first-article dimensional sign-off before the machine is released to production [S3][S5].
The procedure applies to hot chamber machine installations intended for low-melting-point alloys, typically zinc, magnesium, and tin-based compositions, with zinc dominating the commercial machine range from 38 to 168 tons of clamping force [S1][S2][S5].
Process Boundary: What Hot Chamber Commissioning Actually Covers
Hot chamber die casting is a metal forming process ideal for high-volume production of small, intricate parts, with molten metal held ready in an integrated pot within the machine so the plunger can inject it directly into the die [S1]. Because the furnace, gooseneck, and injection plunger are immersed in molten metal, commissioning checks must validate the thermal loop, not just the clamp and shot hydraulics [S2].
The boundary is narrow: low-melting-point alloys only. Marcus Manufacturing states that hot chamber equipment suits zinc, magnesium, and tin alloys, while cold chamber equipment is required for higher-melting-point aluminum alloys [S2]. Forcing an aluminum program through a hot chamber envelope is a process-fit failure that no amount of commissioning can rescue, and it belongs in a different machine review [S5].
A useful reference for the wider context is the Hot Chamber Die Casting Machine: Working Principle and Spec Map article, which maps the gooseneck, nozzle, and clamping subsystems that commissioning must prove out.
Pre-Power Checks: Mechanical, Hydraulic, and Safety Locks
Before any hydraulic energizing, the commissioning engineer walks the machine with the lockout/tagout (LOTO) procedure applied and confirms tie-bar integrity, platen parallelism, ejector stroke, and die-height adjustment across the full thickness window. For the DM38T to DM168T zinc range, die thickness windows run 120-300 mm to 130-430 mm respectively, and tie-bar spacings from 300 x 280 mm up to 400 x 400 mm, so the die envelope must clear the smaller machine's daylight before any further step [S5].
Safety-circuit verification includes the dual-palm guard interlock, die-height motor over-travel limits, shot-end position switches, and emergency-stop response time. Hydraulic pre-fill is done with the reservoir at the OEM-specified level and filters inspected, since hot chamber machines run oil temperatures that share the cell with molten-metal hardware; oil contamination is a direct production risk.
Only after mechanical dry-cycle counts (typically 50-100 empty cycles) and hydraulic ramp to 30%, 60%, and 100% of rated pressure without alarms does the procedure advance to thermal steps [S3].
Hot-End Thermal Commissioning: Gooseneck, Nozzle, and Pot
The gooseneck, nozzle, and integrated pot are the components that distinguish a die casting machine in hot chamber configuration. They must be preheated to the alloy's working temperature in a controlled ramp, typically 60-90 minutes for zinc, to avoid thermal shock to the cast iron gooseneck and to stabilize the immersion depth of the plunger [S3].
Thermocouples are verified at the pot, gooseneck neck, and nozzle tip; the set points are checked against the alloy supplier's data sheet. The Federal Group describes the sequence as preparation, melting, injection, solidification, and ejection, with the melting crucible held in the hot chamber itself, so thermal stability is a process input, not just a machine input [S3].
During this phase, the immersion depth of the plunger is set so that the suction port stays below the bath surface at the lowest expected metal level, and the nozzle seating is checked for cold-shut evidence once the first shots are made.
Shot-Weight and Clamping-Force Calibration
Shot weight is calibrated with the actual production alloy, not a substitute. The DM38T through DM168T specification ladder shows listed zinc shot weights from 0.7 kg at the 38-ton model up to 2.1-2.86 kg at the 168-ton model, and shot capacity does not scale linearly with clamping force because the injection package changes between model families [S5].
Calibration steps: (1) set the slow-shot to bring metal to the nozzle without entrapping air, (2) advance to high-shot and adjust intensification pressure until the cast slug weight matches the calculated biscuit plus cast part weight within +/- 1.5-2%, (3) verify multi-cavity balance by weighing each drop, and (4) record the actual peak intensification pressure for the quality file [S3].
Clamping-force verification is done with the die mounted and a pressure-pin or strain-gauge load cell between the platen and a calibration block. The reading at the machine's stated tonnage must match the rated kN within OEM tolerance; for the 380-1,680 kN range across the five-model ladder, this is the single most important commissioning datapoint for safe production [S5].
First-Article Inspection and Process Window Sign-Off
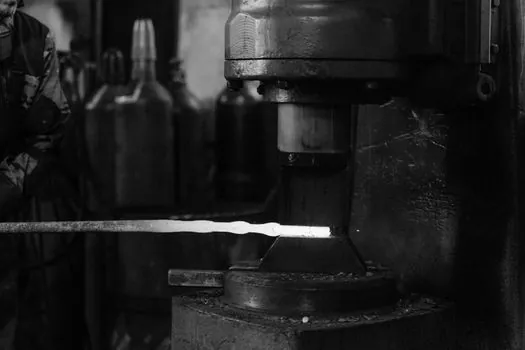
With the alloy molten, the hot end at temperature, and shot/clamp numbers logged, the machine runs a minimum of 50-200 consecutive shots to bring the thermal mass of the die to steady state. First-article inspection covers dimensional critical-to-quality (CTQ) features, weight, surface finish, and a metallurgical cut for porosity on a representative coupon [S3].
The process window is then locked: slow-shot position, fast-shot velocity, intensification pressure, die-spray interval, cycle time, and cooling-water flow rates per circuit. Dynacast's published figures cite proprietary multi-slide hot chamber aluminum capability at up to 10 cycles per minute, and zinc programs typically sit in the same high-throughput band, so cycle time is a sign-off parameter, not a casual observation [S1].
For comparison, a die casting machine failure modes reference is useful during first-article review, because cold-shut, flash, and solder defects are early indicators that the commissioning window was too loose.
Commissioning Limits and Common Failure Modes
The hot chamber envelope has hard limits. Cycle time advantages versus cold chamber configurations come from integrating the furnace and machine, but that same integration means any leak at the gooseneck, nozzle, or plunger packing is an immediate safety event with molten metal present [S2][S3].
Common commissioning failures include: (1) insufficient preheat leading to gooseneck cracking, (2) shot-weight drift as the die heats up and metal density changes, (3) porosity traced to entrapped air from an incorrectly set slow-shot, and (4) flash from a clamping force below the injection pressure peak, especially on long, thin projections [S3][S7].
Alloy-specific caveats matter. AM60 magnesium HPDC studies show that process parameters directly affect porosity and mechanical properties, so the commissioning sign-off window is the baseline for any subsequent optimization, not a one-time gate [S7].
Documentation, Training, and Handover
Commissioning closes with a signed commissioning dossier: the as-built hydraulic and electrical schematics, the calibrated shot/clamp table, the first-article inspection report, the CTQ dimensional layout, the preventive-maintenance schedule for hot-end components, and the operator training record [S3][S5].
Operator training covers the specific safety posture of immersed-bath machines, including the higher baseline risk from molten metal always being present in the working cell, and the maintenance of the gooseneck, nozzle, and plunger packing on the OEM-recommended interval [S1][S2].
Two signals to track after handover are: (1) first-week scrap rate against the first-article baseline, and (2) gooseneck and nozzle replacement interval in production cycles, both of which indicate whether the commissioning window was set conservatively enough for the actual production mix.
Component reference pages worth checking: aluminum die casting machine.