Industrial flooring in prefabricated construction projects is selected against seven criteria, not brand: substrate moisture/alkalinity, point and distributed load, chemical exposure, thermal cycling, slip resistance, install window, and life-cycle cost, per industry guidance [S2][S5].
Polyurethane cement and resin-based epoxy systems remain the dominant heavy-duty choices for manufacturing zones, while LVT, laminate, and modular carpet tile are specified for prefabricated interior overlays in offices, schools, and healthcare pods [S3][S4].
Selection Criteria: Substrate, Load, Chemical, Thermal
Concrete substrate moisture and alkalinity testing is the first gate in any industrial flooring spec, because adhesive failure from out-of-tolerance pH or relative humidity is a primary cause of flooring breakdown on prefabricated slabs [S5]. Heavy-duty resin floors are required to deliver high compressive strength to support forklifts, cranes, and static racking without sinking or cracking under point loads [S2]. Chemical resistance to fuels, lubricants, acids, and aggressive cleaning agents separates resin flooring from LVT and laminate, which lack comparable solvent resistance [S2][S3]. Thermal-shock stability is the deciding factor between epoxy and polyurethane cement: standard epoxy can soften under sustained high heat, whereas polyurethane cement tolerates wider thermal cycling and steam-clean regimes typical in food, beverage, and metalworking prefab modules [S2].
Material Comparison: Epoxy, PU Cement, LVT, Laminate, Polished Concrete
On a four-criterion comparison, epoxy scores high on chemical and abrasion resistance but rates medium on thermal shock and install speed; polyurethane cement scores high on thermal shock and chemical resistance with medium-to-high cost; LVT scores high on install speed and cost but low on load and chemical resistance; polished concrete scores high on load and life-cycle cost but low on slip resistance without aggregates [S2][S3][S6]. Laminate wood is positioned as a cost-effective, scratch-resistant option for office and showroom prefab interiors where chemicals and forklift traffic are absent [S3][S4]. The pattern that emerges: resin systems for process floors, LVT/laminate for dry interior overlays, polished concrete for warehouses where budget and durability dominate over comfort [S6].
Slip, Impact, and Aggregate Options
Slip resistance on resin floors is engineered, not inherent, and is delivered by broadcasting quartz sand, aluminium oxide, or bauxite aggregates into the topcoat to raise surface traction in wet or oily zones [S2]. Impact resistance is the second hard filter: a floor that chips under dropped tooling creates recurring repair costs and trip hazards, so impact-rated resin systems are typically specified above 6 mm thickness in heavy-manufacturing prefab cells [S2]. For high-traffic commercial prefab interiors, durable laminate and heavy-duty vinyl plank are the typical scratch- and water-resistant choices, with the caveat that neither is rated for chemical or forklift service [S3].
Fit-for-Purpose Mapping by Prefab Zone
Process and manufacturing modules in a prefab plant should default to polyurethane cement or heavy-duty epoxy with aggregate broadcast, not LVT, because no LVT product is rated for sustained chemical, thermal, or forklift exposure [S2]. Office and admin pods inside the same prefab complex can use LVT, laminate wood, or modular carpet tile to control cost and acoustic performance without exposing those materials to process loads [S3][S4][S5]. Healthcare and clean-room prefab pods typically select sheet linoleum or seamless epoxy with anti-microbial topcoats, since both tolerate aggressive cleaning chemicals and rolling equipment [S3]. For comparison, schools and education prefabs mix LVT, terrazzo, and carpet tile by room function, with no single material covering gym, hall, and classroom duty simultaneously [S5].
Prefab-Specific Constraints: Lead Time, Modularity, and Substrate
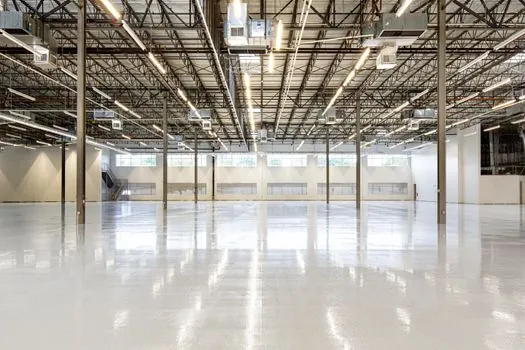
Prefabricated construction compresses flooring decisions into a factory schedule, so material lead time, panel-size constraints, and cure window dominate over field tolerance. Resin floors generally need 7-14 days of cure before full chemical or forklift service, which conflicts with tight prefab install windows unless accelerated-cure systems are specified upfront. Moisture and alkalinity testing of the concrete substrate should be a contractual hold-point, not a field judgment, because adhesive failures in prefab modules are costly to rework after panels are stacked [S5]. Manufacturers' published installation guidelines must be the reference document, not generic best practice, since warranty validation depends on following the exact system build-up [S5].
Standards, Testing, and Failure Modes to Track
Heavy-duty industrial floors are typically specified against Floor Flatness (FF) and Floor Levelness (FL) ratings for racking and forklift aisles, and against LEED material criteria where government or education prefab modules are involved [S5]. Slip-resistance targets are commonly expressed as a minimum Pendulum Test Value (PTV) or an R-rating under DIN 51130 for oily or wet zones, though the specific threshold should be taken from the project safety spec rather than generic guidance. Common failure modes in prefab flooring are: adhesive de-bonding from high substrate moisture or alkalinity, epoxy softening near heat sources, and aggregate loss in slip-rated resin floors; each is preventable at spec stage, not at install stage [S2][S5]. The mechanical and durability demands of an industrial flooring system for a prefab factory floor differ sharply from an SPC flooring overlay used in a modular office pod, and the specifier should treat them as separate product families rather than substitutes. For a parallel spec example in modular education builds, school flooring selection maps wear-layer and slip criteria by room function in a way that translates directly to prefab classroom pods.
Track these signals through 2026-Q4: manufacturer data sheets for accelerated-cure PU cement systems with sub-72-hour return-to-service, and updates to FF/FL tolerance classes under ACI 117 for prefab panel joints. Resin and LVT subcategory coverage on construction tools and construction machinery and equipment spec pages is also a useful cross-check for substrate-prep tooling, since grinder and shot-blast selection drives surface profile before any resin pour.