OSHA 29 CFR 1910.212, the general requirements for all machines, obligates employers to use one or more methods of machine guarding to protect operators and other employees in the machine area from hazards created by points of operation, ingoing nip points, rotating parts, flying chips, and sparks [S3][S4].
Emergency stop devices are a standing OSHA expectation: they must be readily accessible from any operator position, use red actuators on yellow backgrounds per ISO 13850, and remain engaged until manually reset, with no restart of the machine until the actuator is deliberately released [S1][S4].
What 1910.212 actually says, and what it leaves open
29 CFR 1910.212(a)(1) requires that one or more methods of machine guarding be provided to protect the operator and other employees in the machine area from hazards, and that guards be affixed to the machine where possible and prevent hands, arms, and other body parts from making contact with dangerous moving parts [S3][S4].
1910.212 is intentionally short on electrical detail. The substantive emergency stop design rules arrive through NFPA 79-2024 (Electrical Standard for Industrial Machinery), which covers control circuits, emergency stop circuits, and wiring methods, and through IEC 60204-1 as the international equivalent that multinationals routinely dual-design to [S4].
OSHA itself does not prescribe where on a specific piece of equipment an E-stop must be placed; the agency has stated in letters of interpretation that buttons may be located at a variety of positions, provided they are easily accessible to the operator and the stop action does not expose the operator or any other person to a hazard while being activated [S2].
Industry-specific E-stop callouts that do exist in 29 CFR
OSHA's general-duty clause is not the only hook. Specific Subpart O and 1926 rules already mandate E-stops by configuration: belt conveyors in pulp, paper, and paperboard mills under 29 CFR 1910.261(c)(15)(iv) must have an emergency stop cable the full length of the conveyor or conveniently located stop buttons within 10 feet of each work station; screw conveyors at construction sites under 29 CFR 1926.555(a)(3) must use a stop switch that latches the conveyor off and requires deliberate reset to the on or running position [S2].
Other equipment covered by named E-stop requirements in OSHA's standards includes overhead cranes, power-driven guillotine veneer cutters, mechanical power presses (29 CFR 1910.217), and mills and calendars in the rubber and plastics industries [S2].
The practical implication is that a shop running only general light/medium industrial machinery has to build its E-stop program on 1910.212 plus consensus standards, while plants with conveyors, presses, or cranes inherit measurable, citation-ready E-stop rules in parallel.
Design criteria the consensus standards impose on the button itself
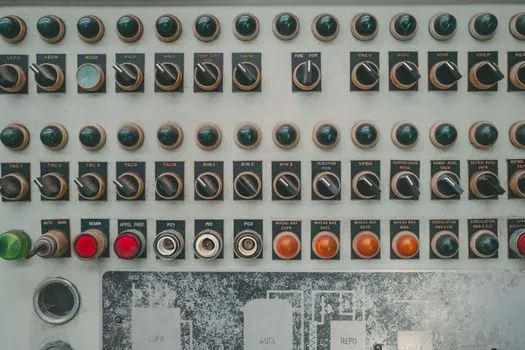
ISO 13850 (the global reference for emergency stop devices) and NFPA 79-2024 Chapter 9 converge on a stable set of hardware expectations: a red mushroom-head or palm actuator on a yellow background, a positive mechanical latching action that holds the contact in the open (stop) state once pressed, and a separate manual reset that returns the machine to a safe state without an automatic restart [S4].
NFPA 79-2024 also addresses the wiring side: emergency stop circuits are wired into the safety control chain so that opening the E-stop contact drops power to the machine actuators through a safety relay or safety PLC, not through a general-purpose contactor alone, and the stop function must remain operative even if a single fault occurs in the control circuit [S4].
On labeling, the device must be clearly marked, easily visible, and identifiable as the emergency stop, with periodic functional testing logged as part of the emergency stop device program, not left to a visual check only [S1][S3].
Placement, accessibility, and the obstruction problem
OSHA's enforcement record treats E-stop placement as a function of operator reach: the button must be within easy reach of every operator station that can actuate a hazardous motion, with no obstruction, no part bin stacked in front, and no fixture blocking the actuation path [S1][S3].
One cited Midwest automotive stamping incident illustrates the failure mode: a press operator's nearest E-stop was physically obstructed by a parts bin at the moment of injury, and OSHA levied $1.2 million in willful and repeat citations under 29 CFR 1910.217 and 1910.212 in part because the obstruction was not flagged during any documented inspection [S3].
For long conveyor lines, the same logic drives the 10-foot station spacing rule in 1910.261 and the pull-cable alternative; for a single machine, the rule of thumb is an E-stop at each operator station and at any ingress/egress point where an operator could become trapped against a hazard [S2].
Inspection cadence: what an audit-defensible schedule looks like
OSHA does not publish a single mandated E-stop test interval, but enforcement actions and CMMS data sets converge on a layered cadence: a documented functional test of every E-stop on a fixed schedule (commonly quarterly to annually depending on environment and severity), a visual accessibility check at every shift handover, and an immediate re-test after any maintenance event that touches the safety circuit [S1][S3].
OSHA's published Safeguarding Equipment and Protecting Employees from Amputations guidance recommends documenting that testing, recording results, and training every operator on E-stop locations, so a missing log entry is treated as evidence that the test did not occur, not that it occurred informally [S2][S3].
For an emergency stop button inventory of a few hundred devices across a plant, the realistic sustained workload is on the order of minutes per device per test cycle, dominated by walk-time to each station, which is why a CMMS-managed schedule with barcode-triggered checklists is the standard mechanism plants use to reach the 97% interlock-test compliance figure that published CMMS deployments report [S3].
Cost of non-compliance and what citation patterns look like
Per-violation OSHA penalties have been published in the $14,000-plus range for serious machine-guarding electrical violations, and willful or repeat citations compound quickly; a single press line with two failed interlocks, one obstructed E-stop, and an undocumented light-curtain bypass was cited for $1.2 million as one enforcement package [S3][S4].
BLS data cited by safety-engineering sources put annual workplace amputations from unguarded machinery at roughly 4,000 and machine-related fatalities in the high hundreds to low thousands per year, which is the exposure envelope OSHA uses to justify treating guarding and E-stop provisions as top-10 most-cited standards [S3].
The dominant recurring findings in 1910.212 citations are not absent E-stops but rather (a) obstructed or non-functional E-stops, (b) interlocks that fail functional test without corrective action, and (c) light curtains or two-hand controls bypassed for production and never logged back into service [S3].
What a defensible 1910.212 E-stop program contains
A program that survives an OSHA audit typically has six elements: a written risk assessment per ISO 12100 or equivalent identifying the required stop categories per ISO 13850; a hardware specification aligned with NFPA 79-2024 Chapter 9 and ISO 13850; a per-station placement map with measured reach distances; a CMMS-tracked functional-test schedule with date, tester, result, and corrective-action closure; a bypass-permit system for any temporary disabling of an interlock or presence-sensing device; and operator training records that name every device, its location, and the reset procedure [S1][S3][S4].
Two operational rules follow from that stack. First, E-stops are wired to the safety control chain, not the standard I/O, so a single wiring fault cannot disable the stop function. Second, no bypass of an interlock or E-stop is ever installed without a logged permit that names a deadline and a restoring action, because the difference between a temporary bypass and a permanent undocumented hazard is, in OSHA's view, exactly the difference between a fixable citation and a willful one [S3][S4].
The next signal worth tracking is OSHA's National Emphasis Program on amputation hazards and any 2026 updates to the Safeguarding Equipment and Protecting Employees from Amputations guidance document, both of which set the inspection checklist inspectors carry into general-industry audits and therefore define the de facto compliance bar for 1910.212 E-stop programs through 2026 [S2][S3].
For component-level specifications, see construction machinery and equipment.
See also our earlier report, P20 vs 1045 Steel: How to Pick the Right Mold Base Plate Grade.