A collapsible crush sleeve is a controlled-yield spacer that sets pinion bearing preload by axial deformation: as the pinion nut is tightened, the sleeve yields a known amount, clamping the inner and outer pinion bearings against their races. Target rotating torque is roughly 8-20 in-lbs with new bearings and around 8 in-lbs on used bearings, while pinion nut torque commonly lands between 160 ft-lbs and 200 ft-lbs on Dana 30, Dana 35, and similar light-duty solid axle housings [S1][S3][S4].
The same sleeve fixes the pinion gear's axial position relative to the ring gear: under acceleration the pinion tries to walk out of the housing, under deceleration it tries to walk in, so the sleeve's compressed length defines the gear mesh depth [S3]. This dual function, preload plus stack-height control, is why crush sleeves are specified as single-use in most rebuild kits and why a pinion crush sleeve replacement is bundled with gear set and bearing work rather than treated as an optional wear item.
How the Sleeve Generates Preload
The pinion stack-up on a typical solid axle runs: pinion flange, pinion nut, outer pinion bearing, pinion gear, inner pinion bearing, crush sleeve, with the sleeve sandwiched between the inner bearing and a shoulder in the housing. As the nut is drawn down, axial force on the inner bearing cone pushes against the sleeve, which yields plastically and shortens, transmitting reaction force back to the outer bearing cone through the gear [S3][S4].
Because the sleeve is a one-shot yielding element, the relationship between nut torque and resulting preload is statistical rather than exact: the same nut torque can produce different compressed lengths on different sleeves, which is why the rotating drag of the pinion, measured with an inch-pound wrench on the nut or on the yoke, is the actual acceptance criterion [S3]. Field reports show sleeve height varying by roughly 0.035 in between a brand-new and a previously crushed sleeve in the same Dana 35 housing, which is enough to push the pinion out of mesh and produce a coast-side whine [S2].
Target Numbers: Nut Torque, Rotating Drag, and Stack-Up
Across common Dana 30, Dana 35, and GM 8.5 passenger-carrier rebuilds, the working numbers cluster in a tight band. Pinion nut torque: 160-200 ft-lbs, with 160-180 ft-lbs common on Dana 30/35 [S1][S3]. Rotating drag on the pinion: roughly 20 in-lbs with new bearings, dropping to about 8 in-lbs on reused bearings; side-bearing preload adds roughly 10 in-lbs to the reading once the carrier is in place [S3][S5].
Sleeve length change during crush is small, on the order of 0.020-0.060 in total, and the failure-mode threshold is narrow: under-crush leaves bearing slop and a driveline clunk on tip-in, over-crush drives the bearings into thermal runaway and seizes them within a few hundred miles [S1][S6]. A common field shortcut on a Dana 44 rear is to skip the sleeve entirely and use solid spacers plus shims for the same function, trading the one-shot convenience of a sleeve for a shim stack that can be re-dialed during a seal change [S1][S6].
Crush Sleeve vs Solid Spacer Plus Shims
The two methods solve the same geometry problem with different trade-offs, and which one a housing uses is often a factory decision rather than a technician choice. Dana 44 rears on Jeep applications are commonly shimmed from the factory, while Dana 30 and Dana 35 fronts and rears use crush sleeves; a Ford 9 in is sleeve-equipped in OE form but is a popular candidate for shim conversion by builders who service their own pinion seals [S1][S3][S6].
Criteria-based comparison of the two pinion-stack arrangements: (1) Field serviceability on a seal change, shimmed housings win because the preload stack is re-dialable, while a sleeve must be replaced and the nut re-torqued from a known reference point. (2) Setup tolerance, sleeve systems are forgiving because the sleeve yields to whatever nut torque is applied, shim systems require a measured stack to within roughly 0.001-0.002 in to hit preload. (3) Cost per rebuild, a sleeve runs a few dollars bundled in a kit, shim kits require a full selection of shim thicknesses. (4) Sealed-unit integrity after service, a shimmed housing returns to a documented stack; a sleeve-only housing depends on the technician's mark of the original nut position plus typically an extra 1/16 turn if nothing else has worn [S1][S3][S6].
Failure Modes and What They Look Like in the Field
Under-crush is the more common of the two failure modes and tends to show up as a clunk on direction changes and a whine that changes with load, sometimes present on coast only, sometimes on drive only, depending on which bearing lost preload [S1][S2][S3]. A documented case on a Dana 35 with a 4.11 gear swap showed a brand-new sleeve from the rebuild kit leaving roughly 0.035 in of yoke end-play after 20 miles of road testing, with a coast-side whine; the original sleeve, refit with no other changes, ran quiet, which points to a sleeve whose as-supplied length was outside the housing's crush window [S2].
Over-crush shows up as heat: bearings run hot, gear oil turns dark quickly, and a hand on the housing cover after a short drive will find it too hot to hold. The reported threshold is roughly 200 ft-lbs of nut torque with no sleeve in the stack, which over-preloads the pinion bearings far past the 20 in-lbs drag target and burns them out within miles [S3]. For routine setup work on a bench or in a vehicle, the same inch-pound measurement discipline that drives pinion setup also drives hydraulic test actuator setup for bench torque verification, where the controlled-yield element under test is the actuator's internal friction rather than a crush sleeve.
Service Procedure: Seal Change vs Full Rebuild
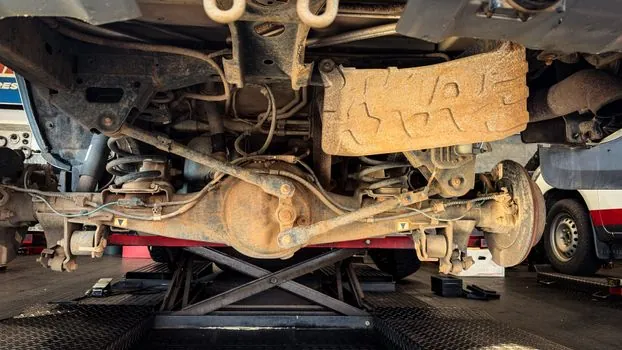
A pinion seal-only change, with the pinion bearings and gear set left in place, can be done in two ways depending on whether the housing is sleeve- or shim-equipped. On a shimmed Dana 44 rear, the seal comes out and a new seal goes in with no preload change; on a sleeve-equipped Dana 30 or 35, the standard shop procedure is to file-mark the pinion nut and the end of the pinion threads before removal, then re-install the nut to the same position plus roughly 1/16 turn (about 0.020-0.030 in of additional nut travel), with the rotating drag rechecked on the yoke [S1].
On a full gear change or pinion bearing replacement, the sleeve is treated as a one-time part: the new sleeve is crushed by tightening the pinion nut to spec, rotating drag is checked with an inch-pound wrench on the yoke until the drag reads in the 8-20 in-lbs band, and then the pinion is spun with an impact wrench to seat the bearings, after which the drag is re-checked [S3][S4]. If a new sleeve will not reach the drag spec at the maximum recommended nut torque, that is a stop-work condition: either the sleeve is wrong for the housing, or the bearings, races, or shim pack are out of spec, and forcing the nut past spec will burn the bearings [S2][S3].
Standards, Common Axles, and Selection Notes
There is no public SAE or ISO standard that pins down crush-sleeve dimensions or preload values across the industry; the numbers are OEM-specific and live in axle-service manuals from Dana, GM, Ford, and Chrysler, plus aftermarket suppliers such as Yukon Gear & Axle and USA Standard Gear that publish their own rebuild specs [S4]. The rotating-drag band, however, is consistent enough across Dana 30, Dana 35, Dana 44, GM 8.5, and Ford 9 in housings that the 8-20 in-lbs target is a reliable cross-axle rule of thumb when no manual is at hand [S3][S5].
For a technician deciding between reusing a sleeve and installing a new one, the practical split is: if the pinion stack was disassembled past the nut, replace the sleeve; if only the seal and yoke came off and the original nut position is markable, a measured re-torque to the same position plus 1/16 turn is field-accepted for a one-time seal service [S1][S2][S3]. For workshop torque hygiene on the inch-pound reading itself, the same discipline used in DKD-R 6-1 calibration sequences for pressure gauges, dwell, repeat, and a known reference, applies to the inch-pound drag check on a freshly set pinion. The two trackable signals going forward are whether axle-service manuals move from sleeve to shim stacks on the Dana 30/35 family in the next product refresh, and whether aftermarket sleeve suppliers tighten the as-supplied length tolerance below the roughly 0.035 in field-reported variation that today forces a trial-fit on a proportion of installs [S2].
For component-level specifications, see shaft collar, and shaft coupling.