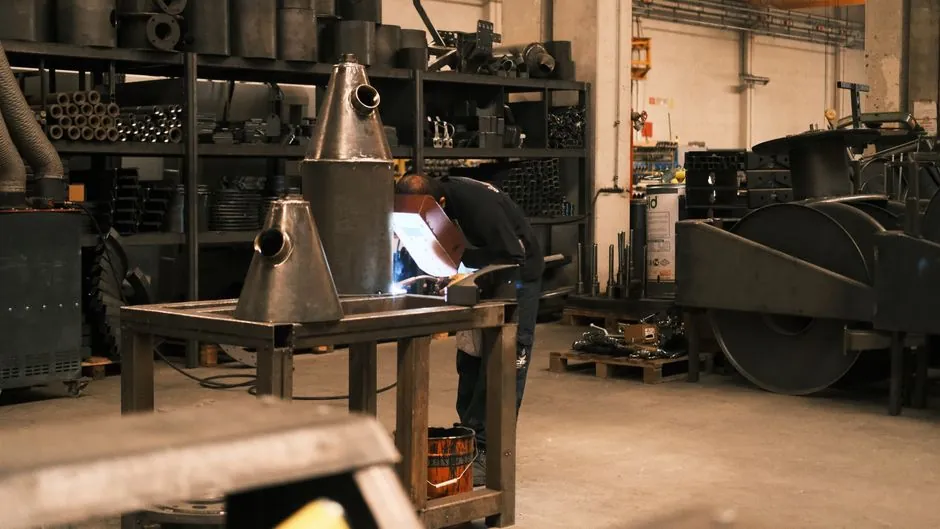
Continuous-production welding plants are sized off the 60% duty-cycle secondary current, not the kVA nameplate; SAIL's IPSS 1-07-001-95 calls out 400 A and 600 A transformer ratings with dual continuous control at 415 V +6% as the plant-side reference points [S3].
The transformer inside a welding machine is a step-down unit that takes 208-600 V primary at 15-55 A and delivers up to 80 V secondary at currents that can reach 1000 A AC depending on the process, with the secondary current level directly driving the core size and overall mass of the unit [S2].
What "Transformer Rating" Actually Means on a Welding Plant
The kVA on the nameplate of a single-phase 25 kVA welding transformer at 240 V draws roughly 104 A full load, and at 208 V the primary current rises to about 120 A, which is the number plant electricians need for feeder sizing rather than the kVA figure [S1]. Welding power supplies are predominantly controllable transformers, not generators, and they are categorised as constant current (CC) for SMAW and GTAW or constant voltage (CV) for GMAW and flux-cored work, with the transformer design choice locked to that control mode [S4].
Industrial ratings on the SAIL IPSS document are written as 400 A and 600 A current ratings with dual continuous control, with 415 V +6% on the primary and a defined maximum continuous hand-welding current, which makes the duty cycle and the primary tolerance, not the kVA, the binding spec for a multi-station welding bay [S3]. A typical transformer-style supply holds 17-45 V open-circuit and 55-590 A output, with rectifiers added on higher-end units to convert AC to DC for polarity selection [S4].
Selection Criteria: kVA vs. Duty-Cycle vs. Primary Tolerance
Three numbers have to match before a transformer goes onto a plant floor: the secondary current at the rated duty cycle, the primary voltage tolerance band the plant can supply, and the thermal time constant at the station density you actually run. SAIL IPSS 1-07-001-95 anchors the first two at 400-600 A and 415 V +6% with dual continuous control, and the CWB reference covers the secondary envelope at 17-80 V open-circuit and up to 1000 A depending on the process [S2][S3].
On the AC/DC split, DC transformer-rectifier designs give a more stable arc and better penetration control, which is the standard approach for gas tungsten arc work and for any code-critical pipe root pass where arc stability is non-negotiable, while basic AC step-down units remain the lower-cost option for general fabrication [S4][S5]. The Wikipedia survey of welding power supply design also makes the practical point that the first inverter welding supplies appeared in the late 1970s to cut transformer mass, and modern inverter topologies switch on the high-voltage primary side to shrink the magnetics versus switching on the secondary side [S2][S4].
For plants weighing inverter vs. conventional transformer-rectifier, the inverter wins on footprint and weight per amp, while the conventional iron-core transformer typically wins on capital cost, repairability, and tolerance to dirty input power, and that tradeoff is why heavy structural shops still order transformer-rectifier units in the 400-600 A class specified by IPSS 1-07-001-95 [S2][S3]. The related arc welding power source selection guide walks through the AC vs. DC logic in more detail for engineers balancing that decision.
Who the High-Rating Transformer Is For, and Who It Is Not For
A 400-600 A continuous-duty welding transformer is for fabrication shops running multiple stations in parallel on structural steel, pressure-vessel shops doing SMAW and GTAW, and any plant cell where the welding load is the dominant 415 V single-phase load. SAIL IPSS 1-07-001-95 is written explicitly for that class of plant equipment, with current ratings of 400 and 600 A and a continuous-control requirement that maps to multi-arc production use [S3].
It is not for job shops running one or two stick welders a few hours a day, not for field-mobile welding where an engine-driven generator beats a fixed transformer, and not for thin-sheet GMAW work where a compact inverter at lower primary current is the better fit. The Wikipedia entry on welding power supplies points out that mobile engine-driven welding sets exist precisely because the grid is unavailable, while a plant transformer only makes sense where the grid is reliable and the load is sustained [S4].
Comparison: Conventional Transformer vs. Transformer-Rectifier vs. Inverter
The three topologies line up against four decision criteria the way most spec engineers actually buy them: capital cost per amp, mass per amp, arc stability for code work, and tolerance to dirty primary supply. The conventional AC transformer is cheapest per amp and most rugged on a poor 415 V feed, but it is the heaviest and only delivers AC, so DC processes need the next step up. The transformer-rectifier adds a diode bridge to give DC output with a smoother arc, at moderate cost and weight, and is the standard fit for SMAW and GTAW in a continuous-production plant [S2][S4][S5].
The inverter topology switches the primary at high frequency to shrink the magnetics, drops the mass per amp dramatically, and is the usual pick when floor space or mobile use dominates, but it costs more per amp and is more sensitive to input power quality. SAIL IPSS 1-07-001-95 still anchors plant ratings at 400-600 A in conventional transformer-rectifier form, which is why most multi-station plant cells in heavy industry are not inverter-dominated [S2][S3][S4].
Use Cases Drawn from the 400-600 A Class
SAIL IPSS 1-07-001-95 lists the 400 A and 600 A transformer ratings as the standard plant-side sizes with dual continuous control at 415 V +6% primary, which is the document most Indian heavy-engineering plants reference when they spec a new welding bay or a captive fabrication shop for steel structures [S3]. The CWB technical piece anchors the secondary envelope at 17-80 V open-circuit and up to 1000 A, which covers the 400-600 A continuous-current ratings comfortably for hand-welding current at the high end [S2].
Engineers specifying a pipe fabrication cell will pair that transformer rating with a constant-current source for SMAW or GTAW work, since the CC characteristic keeps heat input roughly constant even when the welder's hand drifts and arc length changes, while a GMAW or flux-cored cell needs constant-voltage behaviour and a wire feeder that senses voltage to stabilise the arc [S4]. For pipe root-pass work specifically, the related arc vs. TIG welding for pipe root pass guide covers how the chosen power source interacts with prep geometry and the governing weld procedure.
Limitations, Failure Modes, and Sourcing Constraints
The hard limits on a transformer-rated welding plant are thermal, not electrical: the 60% duty cycle is the thermal envelope, and pushing past it trips the thermal cutout or, on older units, burns the windings. Per SAIL IPSS 1-07-001-95, welding transformers of current rating 400 and 600 A use a dual continuous control system at 415 V + 6 percent [S3].
On a 25 kVA single-phase unit, primary current at 240 V is around 104 A full load and rises to roughly 120 A at 208 V, which is the first failure mode undersized feeders hit when the plant voltage sags under load [S1]. Inverter supplies have the opposite constraint: they are more sensitive to dirty input and to single-phase voltage imbalance, so the upstream power quality has to be audited before an inverter retrofit on an old feeder. The CWB reference is direct that the higher the amperage output, the larger the transformer core and the heavier the machine, which is why floor-loading and crane access need to be checked before a 600 A station goes into an existing bay [S2].
Standards and Reference Documents
The two non-vendor references that plant engineers actually cite are SAIL IPSS 1-07-001-95 for the 400-600 A, 415 V +6%, dual continuous control rating, and the CWB Group's "What is a welding transformer?" technical article for the step-down function and the 208-600 V primary to 80 V / 1000 A secondary envelope [S2][S3]. The general topology context comes from the Wikipedia welding power supply entry, which classifies units as CC vs. CV and transformer vs. transformer-rectifier vs. inverter [S4]. A vendor-side explainer on DC transformer-rectifier design adds the practical point that DC outputs deliver more consistent arcs for precision processes such as GTAW [S5].
Engineers sizing a transformer for a multi-station plant should keep the SAIL IPSS 1-07-001-95 rating table open alongside the CWB secondary-envelope diagram, and verify the primary feeder can deliver 104-120 A at 208-240 V per 25 kVA station before signing the purchase order [S1][S3]. The next spec watch-point is whether the cell will migrate to inverter supplies as feeder quality improves, since the IPSS document is written around the heavier transformer-rectifier class and most plant retrofits now run the cost per kVA comparison in that direction.
The underlying component specifications are covered under arc welder, concrete batching plant, and welding cutting tool.