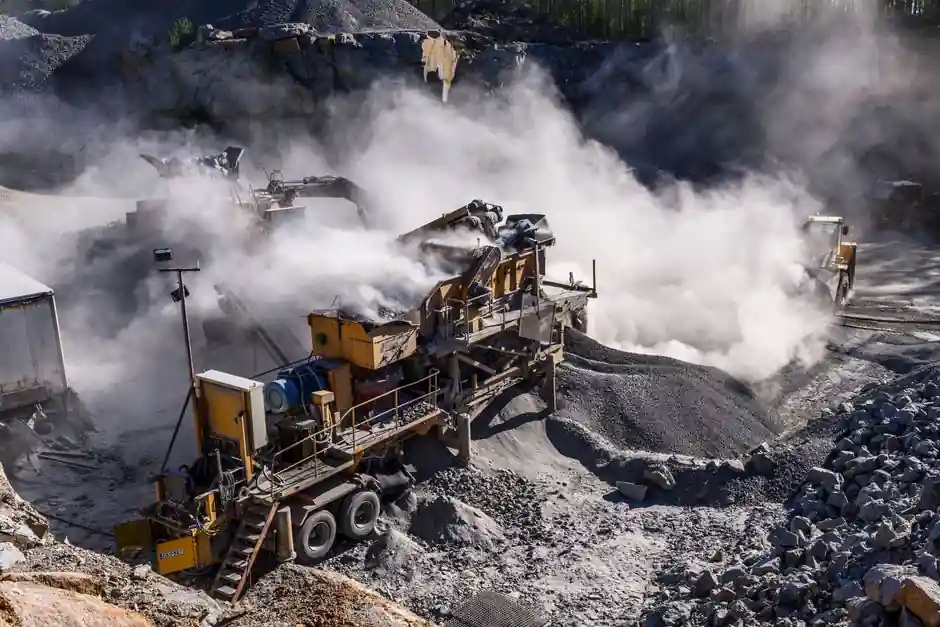
Asphalt pavers working in quarry and aggregate-haul operations live in heat, dust, and sticky residue, and June 2026 maintenance guidance from FieldFix states that paver problems show up simultaneously in the machine and the finished mat, so a single conveyor or screed defect can shut the whole paving train down [S3]. The cost is rarely just the part: a mid-pull stoppage also drops mix temperature, burns labor, and stacks trucks while traffic control is still being paid for [S3].
Fleets that get consistent mat quality treat the paver as a production AND finish machine, with screed cleanliness, conveyor tension, and auger flight condition checked every shift rather than after a failure [S3]. The maintenance profile differs from a hydraulic excavator or crusher, because thermal load, asphalt adhesion, and screed plate wear accelerate beyond what standard construction-equipment PM intervals assume.
Daily Pre-Shift Inspection: What Has to Be Touched, Not Just Looked At
A pre-shift walkaround must cover engine oil, hydraulic fluid, coolant, fuel system, and brake fluid gauge levels, plus a hands-on check of belt condition, hydraulic hoses, engine filters, and battery connections before any truck dumps into the hopper [S4]. Pavers run hot by nature, so the radiator, hydraulic cooler, and air filter should be cleared of dust and bitumen residue, and the operator must verify control functions, gauges, backup alarms, and work lights are functional, not just present [S3][S4].
Hopper inspection, conveyor slat check, auger flight inspection, and screed plate condition form the second tier of the daily routine, because these are the components that translate machine health into mat quality [S2][S3]. The asphalt paver class generally uses hydrostatic drives that share the hydraulic reservoir with the vibratory screed circuit, so low hydraulic fluid on a hot day starves the screed first and shows up as ripples before it triggers an alarm. For a complete daily routine, see the HVI pre-shift paver checklist workflow, which lists fluids, hydraulics, screed, conveyor, and safety systems as non-optional items each shift [S2].
Conveyor, Auger, and Screed: The Three Components That Decide Mat Quality
A conveyor failure stops material flow at the back of the paver and backs up the entire paving operation within minutes, which is why chain tension, slat condition, and the tail-pulley bearings are weekly-touched items, not annual ones [S3]. A neglected chain does more than wear out: it throws off material head in front of the screed, causing the auger to starve or overfeed, and the result is a wavy mat that no roller pattern can fix [S3].
The screed is the single most mat-defect-sensitive assembly on the machine. Laser-controlled thermometers should be used to monitor screed plate temperature during transport and on-site, and the screed must be covered to retain heat between pulls, because temperature drop across the plate directly causes segregation and tearing at the start of every stop [S4]. Crown setting, extension alignment, plate straightness, and tamper-bar wear all need verification, and a test run on a sacrificial section is the standard pre-pour check before any production paving begins [S4].
Auger flight wear and bearing temperature are the third mat-defect driver; uneven auger speed or worn flights create a chevron pattern in the mat that compacts into permanent surface defects [S3]. In quarry-side operations, where the mix often contains harder aggregate fractions, auger and conveyor wear accelerate, and the inspection interval for flight thickness should be tightened versus highway paving.
Hydraulic System, Cooling, and Burner Care: The Hidden Failure Modes
Hydraulic oil level and condition control both the propel system and the screed lift/extend circuit, and low fluid or contaminated oil shows up first as slow or jerky screed response, not as a hard fault [S1]. The hydraulic cooler and radiator must be kept clean because asphalt pavers run hot by nature, and a plugged cooler stack elevates oil temperature past 90 to 95 degrees C in normal ambient, which degrades seal life and shortens hydraulic-fluid drain intervals [S3].
The screed burner system, whether electric or diesel-fired, is a primary mat-defect source when neglected. Clogged burner nozzles, weak ignition electrodes, and propane/ diesel supply faults cause cold streaks across the screed plate, and the mat pulls with visible tearing exactly where the plate is under-temperature [S3]. A simple burner test at pre-shift, watching for even blue flame across all sections, is a higher-value check than many operators perform.
For fleets running automated grade and slope controls, the sensors and hydraulic proportional valves that drive them sit in the dust and heat envelope of the screed, and they degrade on roughly the same timeline as the screed wear plates. Calibration drift on grade sensors can mimic a screed setup problem, so the maintenance program has to cover both. The sensing and control elements are conceptually similar to those used in a pressure transmitter loop on a process skid, where contamination and thermal cycling drive the failure pattern, even though the physical sensor type is different.
Weekly and Monthly PM: Cleaning, Track Tension, and Off-Season Storage
Weekly routines must include deep cleaning of the undercarriage, tracks, screed, filters, and engine compartment, because accumulated bitumen hides wear patterns and accelerates corrosion on steel surfaces [S1][S5]. Track tension should be measured, not eyeballed: tracks that are too loose cause stability and steering problems on uneven quarry bench surfaces, while over-tightened tracks accelerate idler and sprocket wear [S1].
Monthly intervals typically include hydraulic fluid sampling, conveyor chain elongation measurement, auger bearing grease analysis, and screed plate thickness gauging, with the data trended against mat-quality records from the same period [S3]. Off-season storage requires a full clean-down, fuel stabilization, battery removal or float-charge, and screed plate protection, because a single season of neglect during layup can wipe out a year of careful daily checks [S5].
Documented maintenance logs are a force multiplier: fleets that pair daily paver inspection records with mat-density test results can correlate a maintenance miss with a quality miss within a shift, and the cost of a digital inspection app is dwarfed by the cost of one milled-and-replaced lane [S2][S3]. The link between hydraulic cleanliness, sensor stability, and finished-mat consistency is the same logical pattern seen in flow meter calibration on a process line, where the sensor drift shows up as product drift long before it shows up as an equipment alarm.
Common Failure Modes and When to Repair vs Replace
The most expensive paver failures in quarry use cluster around five modes: conveyor chain stretch or breakage, screed plate wear or cracking, auger flight wear, hydraulic hose blowouts, and burner failure [S3][S4]. Of these, conveyor and screed failures are the only ones that immediately stop a pull, while auger and hydraulic issues degrade mat quality before they stop production.
Repair-versus-replace thresholds follow component cost relative to rebuilt exchange. A screed plate can be re-machined once or twice before the cross-section is too thin to hold heat, at which point replacement is mandatory rather than optional [S3]. Conveyor chains can be re-tensioned and individual slats replaced, but once elongation exceeds the manufacturer's limit (commonly 3 percent over nominal pitch), the chain is a throw-away item regardless of visual appearance.
Hydraulic hoses should be replaced at first sign of outer-cover abrasion, not at burst, because the failure mode is fast and the contamination cost to the rest of the hydraulic system can exceed the hose cost by an order of magnitude [S1]. For screed wear components and burner nozzles, OEM service intervals are conservative and worth following rather than extending, because the cost of an unplanned screed replacement mid-shift is roughly an order of magnitude higher than a planned nozzle change.
Sourcing, Standards, and Sourcing Signals for Quarry-Side Paver Fleets
Quarry and aggregate-haul operations should source pavers with Tier 4 Final diesel platforms where regulatory, and prioritize hydrostatic drive and modular screed designs for parts commonality across the fleet [S5]. Where paver uptime drives truck-cycle economics, a small stockpile of high-wear items (conveyor slats, auger flight sections, screed wear plates, and burner nozzles) is a lower-cost insurance policy than any service contract.
For the wider maintenance program, the same logic of pairing sensor data with equipment data applies whether the equipment is a paver, a PLC on a crusher line, or an industrial valve on a bitumen-loading skid: the failure is visible in the process data before it is visible to the operator. Fleet managers running mixed paver and crusher maintenance programs in the same quarry are increasingly using digital inspection platforms to consolidate daily checks, fuel logs, and parts inventory across both [S2].
The next trackable signal is whether 2026 model-year pavers ship with onboard mat-quality telemetry as a standard option, since that would close the loop between screed condition, sensor data, and finished-mat density in a single dashboard. A second signal is whether burner-electric (rather than diesel-fired) screed heat becomes more common in Tier 4 Final platforms, because it removes a primary mat-defect and emissions source at the same time.
Background reading: EV Charging Station Manufacturing Cost: BOM, Drivers, and Margins.