
An Arkansas hot-strip mill now moves about 1,000 steel coils (≈30,000 tons) per day using three unmanned overhead cranes with thermal imaging cameras and laser positioning systems that report each crane's exact yard location [S3].
Paper and pulp plants specify a different class of automated overhead crane, with A6–A8 FEM/ISO duty ratings, IP65-sealed electrical panels, and 30–80+ ton lifting capacity for parent rolls on continuous 24/7 lines [S5]. The two deployments share a control philosophy but diverge sharply on duty cycle, payload class, and environmental protection.
Steel mill coil yard: thermal imaging, laser positioning, rules-based dispatch
The Arkansas system uses three fully automated overhead cranes working with two coil transfer cars that accept hot coils off a walking beam from the hot mill, with all motion controlled by Morgan Automation's Cephas logistic management system running a rules-based engine and a custom yard map divided into four destination quadrants [S3]. A typical coil at this yard measures approximately 83 inches outside diameter by 82 inches wide and weighs 28 tons on average, and the cranes are not allowed to move a coil until its thermal camera reading confirms it has cooled enough for handling [S3]. Coil move order is prioritized dynamically from the mill's real-time workflow, and the system logged "zero downtime during the first six months of operation" per the Siemens/Morgan integration [S3].
Drives, PLC, safety I/O, power-quality metering, wireless hardware, and the TIA Portal commissioning platform for this deployment were supplied by Siemens under a long-term motion-control partnership with Morgan Automation [S3]. Reducing outdoor coil storage was a primary stated goal, since indoor storage cuts rust, lowers energy cost from eliminating lift-truck rehandling, and tightens coil-to-coil spacing for denser storage [S3]. A comparable driver applies to metals more broadly: Simmers Crane's automation stack targets accurate positioning, temperature monitoring, and reduced downtime for steel mills and aluminum processing facilities handling coils, slabs, and billets [S2].
Paper mill parent roll handling: A6–A8 duty, sway control, IP65 sealing
Paper and pulp plants run cranes at A6, A7, or A8 work levels per FEM/ISO rules to support 10–20+ lifts per hour across multiple shifts, with parent rolls commonly weighing 30 to over 80 tons handled near winders, rewinders, and pulping vats [S5]. Standard "factory" cranes fail quickly in this service because of corrosion from steam, bleach, and acid or base pulping chemicals, brake thermal cycling from frequent heavy stops, and frame fatigue from repeated high-use loads [S5].
Mill-duty builds add thick epoxy coatings on girders and end trucks, stainless or galvanized components at corrosion-critical points, IP65 or higher sealed electrical panels and motors, and moisture-resistant wiring and connectors [S5]. Sway-stop or no-sway control is a standard requirement because residual pendulum motion at the load damages roll edges and trips safety limits, and a custom spreader beam or vacuum lifter is typically fitted for parent roll handling [S5]. Specialized parent roll handling cranes from Konecranes similarly target reduced damage and precise lifting of heavy paper rolls in production lines, with engineering pitched at production-flow rather than one-off lift duty [S1].
Functional requirements: motion control, obstacle avoidance, and WMS integration
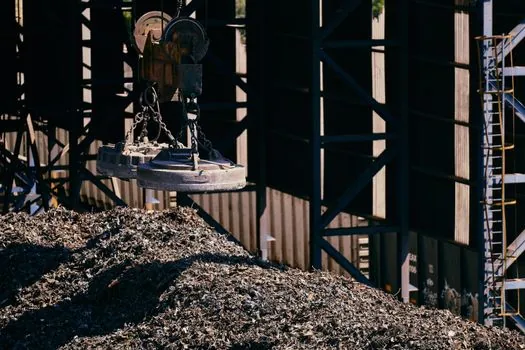
Simmers Crane's automation stack, used in metals and adjacent process industries, layers skew control to minimize travel misalignment, no-sway technology to cut load oscillation at placement, obstacle avoidance to prevent collisions, and coordinated multi-axis moves for compound tasks [S2]. Level 1 crane controls are designed to hand off to a Level 2 warehouse management system, with redundancy features sized for the safety case required in steel and paper service [S2].
AFE Crane offers both semi-automated and fully automated process cranes built on PLC plus VFD architectures for application-specific handling, including explosion-proof overhead cranes for hazardous process areas [S4]. Explosion protection matters in paper bleach plants and in oil-and-gas adjacent yards referenced in the broader automated-crane literature, where vapors or dust require EX-rated hoists and enclosed electrical packages [S6]. A typical specification stack therefore includes an automated motion controller, anti-sway firmware, an anti-collision layer tied to the WMS or yard logistic system, and a rated enclosure (IP65 minimum, EX where flammable atmospheres exist) sized to the mill environment [S2][S5].
Selection criteria: payload, duty class, environment, and yard topology
Four decision criteria separate the steel-coil and paper-roll automated-crane problem statements, and the same criteria pick equipment within either industry:
1) Payload class. Steel coil yards cluster around 25–30 ton average coils with peak lifts up to 40+ tons for the heaviest units; paper mill parent roll cranes are commonly specced at 30–80+ tons with custom spreaders for very large jumbo rolls [S3][S5].
2) Duty cycle. A6–A8 FEM/ISO ratings for paper (10–20+ lifts/hour, multi-shift, 24/7) versus a slower but higher-throughput steady state in steel coil yards handling roughly 1,000 coils/day across three cranes (≈333 coils/crane/day) [S3][S5].
3) Environment. Paper and pulp need IP65+ sealing and corrosion-resistant materials because of steam, bleach, and pulping chemicals; steel mills need thermal imaging and high-temperature-tolerant components for hot-coil staging [S3][S5].
4) Yard topology. Steel yard control depends on a quadrant map and a rules-based engine for deterministic dispatch, while paper mill control depends on winder, rewinder, and pulper line-side positioning and WMS or roll-tracking integration [S3][S2]. The process crane configuration, and the surrounding construction machinery and equipment stack that supports the building structure, runway beams, and transfer cars, are the integration boundary between the crane OEM and the mill's logistic system [S4].
Limits, failure modes, and what the specs do not solve
Automated crane systems do not eliminate the need for daily inspection; Konecranes' CheckApp daily inspection workflow and structured preventive maintenance programs remain a baseline service input even on fully unmanned yards [S1]. The Arkansas deployment itself depended on integrating three vendor stacks (Morgan Cephas, Siemens drives/PLCs/wireless, and laser + thermal sensors), and the headline "zero downtime in six months" claim is tied to that specific commissioning, not to automation in the abstract [S3].
Material and energy trade-offs also remain: indoor storage reduces rust and energy cost from lift-truck rehandling, but it raises the capex envelope for the building and runway steel that supports the overhead conveyor and crane infrastructure feeding the line [S3][S7]. Environmental gains cited for automated systems, including reduced material waste through accurate load handling and placement, are conditional on the WMS or yard-logistic layer being calibrated to the actual lift cycle, not on the crane automation alone [S7]. For process engineers sizing a new build or retrofit, the practical next nodes are a duty-class calculation against the FEM/ISO table for the specific paper or steel line, and a hazard-area classification that determines whether IP65 sealing alone is sufficient or an EX-rated hoist package is required [S2][S5][S6].
Background reading: IEC 60947-5-2 switching distance: Sn, Sr, Sa and the 2019 edition delta.