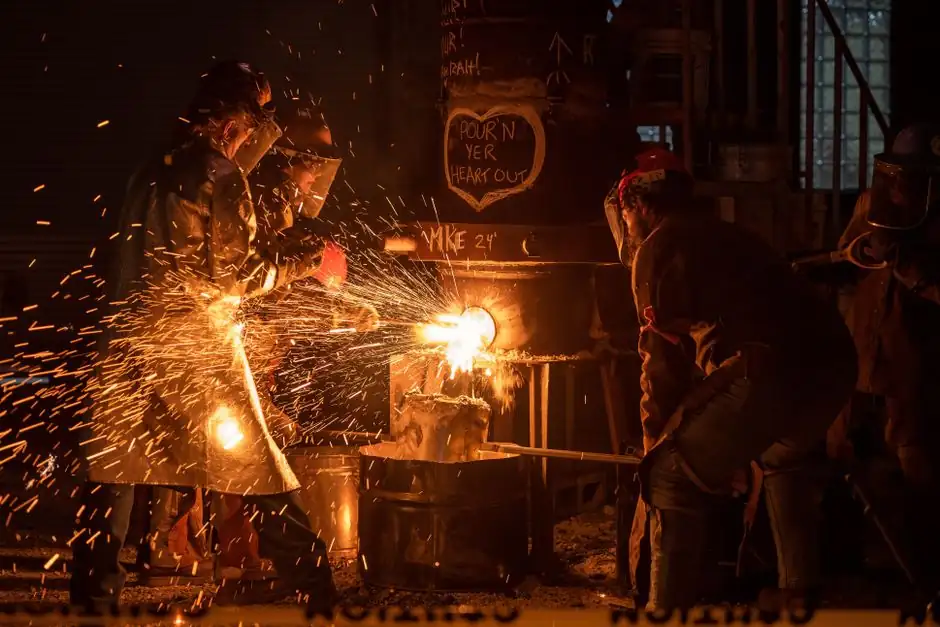
Magnesium fade in ductile iron held in a pressure pour furnace is the steady oxidative and desulphurisation-driven loss of residual Mg from a treated bath, dropping the dissolved Mg toward the roughly 0.04 wt% minimum needed to keep graphite in nodular form [S6]. Once treated, the iron typically has a 12-15 minute window before fading forces the heel to be pigged or refreshed, and continuous holding without intervention is not viable for ductile grades [S1].
The control levers are the bath Mg target, the furnace atmosphere, the lining chemistry, and a deliberate heel-refresh schedule at every weekly start-up, where 5-6 ton "faded" heels with essentially no remaining Mg are routine [S1]. For ductile iron specifically, the problem is sharper than for gray iron because the nodular graphite morphology collapses as soon as Mg falls below the threshold, so fade is not a yield loss, it is a grade-conversion loss.
Why Mg fades faster than Fe or Si in a held ductile bath
Mg has a vapour pressure near 1 atm at roughly 1107 degC, sits well below Fe and Si on the oxide-formation free energy curve, and reacts avidly with any entrained oxygen, sulphur, or refractories-derived silica to form MgO and MgS that report to the slag [S5]. The first loss mechanism is therefore evaporative and reaction-driven, not dilutive: every minute the bath sits under a non-inert cover, Mg is consumed at the surface and at the slag-metal interface [S1].
For ductile iron specifically, this matters because the residual Mg window is narrow. The target residual for as-poured ductile is typically about 0.04 wt%, with the upper limit set by carbide risk and the lower limit by graphite morphology reversion toward flake/vermicular forms [S6]. Once fade pushes the bath below the lower limit, the iron must be either pigged (downgraded to a non-nodular product) or re-treated, which is the economic reason every pressure pour cell carries a refresh alloy on hand [S1].
What the furnace itself does to the fade rate
The furnace vessel is an active participant, not a passive container. Magnesia-bearing slag adheres to the working lining, and that adherent slag is itself a sink for Mg from the bath, so a lining that is already loaded with MgO-rich build-up acts as a continuing drag on residual Mg [S5]. Operators see this as a lining-life / fade trade: a fresh, clean lining will hold a treated bath longer than one that has been conditioning itself with weeks of MgO slag [S3].
The pour-siphon and fill-siphon geometry matters just as much. The PRV-style vertical channel furnace with straight siphons (no bottom-bend) is designed so the fill and pour siphons can be rodded or even exchanged with metal still inside, because Mg, sulphur, and nitrogen deposits build up in those passages and choke flow within 24 hours of continuous service if not cleaned [S2]. That 24-hour cleaning interval is not arbitrary: it matches the observed Mg fade cycle under production conditions, and skipping the rod-out is one of the fastest ways to accelerate fade in the heel that follows [S9].
Atmosphere control: nitrogen cover, vacuum, and what they buy you
Pressurised nitrogen covers are standard on pressure pour ductile cells, and field data shows the cover gas itself has little initial effect on Mg fade, but the post-stabilisation behaviour of an inert cover does reduce the steady-state fade rate enough to keep the bath at pourable Mg content for the full rated holding time of up to 8 hours [S2]. The mechanism is straightforward: nitrogen displaces entrained oxygen and water vapour from the headspace, so the surface of the bath is no longer being fed an unlimited supply of Mg-getters [S2].
By contrast, any cover that admits air (a leaky seal, a hatch left cracked for temperature measurement, a deslagging door not re-seated) accelerates fade measurably. The practical rule on a production cell is that the cover gas pressure and oxygen trim should be logged, not trusted, because the difference between an 8-hour and a 4-hour holding window is often a single failed seal rather than a change in alloy chemistry [S9].
Refractory and slag chemistry as a hidden fade driver
Magnesia-based refractories are the standard working lining for ductile iron pressure pour furnaces, and the MgO-rich slag that builds up on that lining is the same chemistry as the MgO the bath is trying to retain, so the lining is not the villain on day one, but it becomes one as the campaign ages [S5]. Slag adherence analysis from production campaigns shows the adherent composition is mainly magnesia plus entrained iron oxide and silica, with the MgO fraction rising as the lining absorbs Mg from previous heats [S5].
The second-order effect is the interaction between the MgO-saturated slag and the bath: once the slag is MgO-rich, it is at equilibrium with the bath's Mg and stops pulling Mg out, which is why an aged lining is often more stable than a fresh one for fade behaviour, even though it is worse for thermal shock resistance [S3]. The refractory specification for the melt and combustion zones in a ductile iron pressure pour cell should therefore be chosen for slag chemistry compatibility first and thermal cycling second, because the slag is what governs the fade curve [S5].
Refresh alloys: MgFeSi vs Ni-Mg vs Fe-Mg briquettes
Three alloy routes are in commercial use to bring a faded heel back up to pourable Mg without pigging the iron: high-Mg ferrosilicon (typically 9-10% Mg, balance Fe-Si), nickel-magnesium master alloy, and proprietary iron-magnesium briquettes in the 10-15% Mg range [S1]. MgFeSi is the cheapest per unit of Mg added but carries 40-50% Si into the bath, which pushes the final silicon toward the upper spec limit and leaves no room for a post-inoculation silicon addition [S1].
Ni-Mg master alloy trades cost for cleanliness: nickel adds about 0.5-1.0% Ni to the iron (often desirable for pearlite stabilisation or section-size uniformity in heavy castings) and delivers Mg with very little slag and a much narrower silicon bump than MgFeSi, so it is the preferred route in high-tonnage pressure pour cells running ductile grades with tight Si ceilings [S1]. The 10-15% Fe-Mg briquette sits in between: it adds essentially no Si, no Ni, and only a small amount of additional iron, so it is the most forgiving option when the heel chemistry is already near the Si upper limit and the foundry does not want to push the bath out of spec on a single alloy addition [S1]. A common production practice is to size the addition so the heel can be re-treated and poured without an intermediate chemistry check, using the heel mass and an assumed residual of essentially 0% Mg as the worst-case input.
Pouring window, heel strategy, and the 10% Mg target trick
The standard as-treated pour window for ductile iron is 12-15 minutes from MgFeSi treatment, and any metal still in the furnace after that point is, by definition, a candidate for pigging or refreshment, not for direct pouring [S1]. A pressure pour channel furnace running an automated green sand line will always maintain a minimum heel to keep the inductor primed and the metal at temperature, so the heel refresh is not optional, it is a designed-in part of the operating procedure [S1].
One of the more useful process levers is to deliberately lower the per-charge target Mg by about 10% on the assumption that the heel will be harmonised with fresh metal over the holding period, which both reduces the fade rate per minute (lower initial Mg means lower initial vapour pressure driving loss) and trims the MgFeSi cost per ton poured [S3]. The trade is a tighter chemistry margin: if the heel refresh fails or the holding time extends, the bath will drop below pourable Mg faster than it would at the higher initial target, so the lever only works in cells with reliable heel-refresh logistics and consistent holding times [S3].
Failure modes and what they look like on the shop floor
The first sign of uncontrolled Mg fade in a pressure pour cell is a drift in the as-poured Mg check from the spectrometer, typically a 0.005-0.010 wt% drop per hour of holding once the bath has stabilised [S2]. The second sign is a change in the fracture surface of the poured test bar: from the bright, silvery, finely nodular fracture of healthy ductile toward a darker, coarser fracture with visible vermicular or flake graphite patches as the residual Mg crosses the morphology threshold [S4]. The third sign, which usually arrives before the metallurgical signs because it is faster, is a build-up of MgO-MgS dross on the surface of the bath and on the siphon walls, which the pour-siphon rod-out interval is designed to manage on a 24-hour cycle [S9].
For a foundry running a mix of cast iron grades on the same pressure pour line, the cleanest signal is to keep a pour-time log stamped with the bath age and the residual Mg reading, and to treat any heat poured more than 15 minutes after treatment as suspect on chemistry even if the spectrometer passes, because the fade is not always uniform across the heel and the sample probe can miss a depleted surface layer [S8].
Where this leaves a foundry running pressure-pour ductile
Track the 24-hour siphon rod-out interval, the nitrogen cover pressure log, the lining age in MgO-equivalent heats, and the residual Mg trend across the heel over a normal week; those four signals together predict the next fade-driven yield event more reliably than any single chemistry check. For more on the equipment side of this problem, see our guide on the magnesium die casting machine class of equipment, which faces a related (but harder) fade control problem at much higher Mg fractions. For context on how rare-earth and Mg supply chains interact with iron-foundry demand, see the Q3 2026 cerium oxide price outlook and the decade-scale rare-earth recycling assessment. [S2]