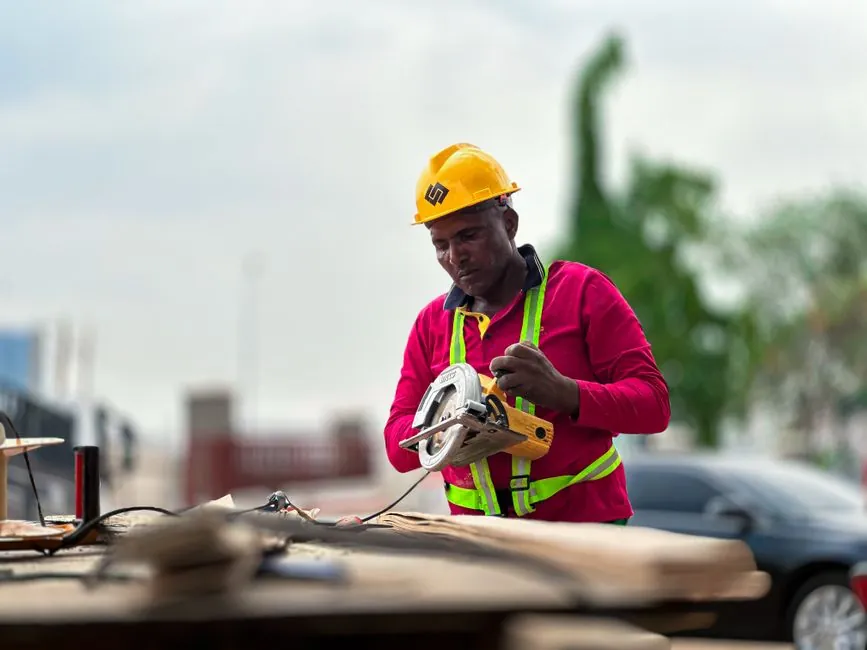
A marble cutter's usable life is governed by diamond segment wear, bond erosion, and steel-core fatigue, with continuous-rim diamond blades typically delivering 80-300 hours of cutting before segment height drops below the 2 mm replacement threshold [S1].
For a 1450 W, 220-240 V corded marble cutter such as the Tolsen 79533, the manual's safety and operating procedures apply across the full service life, and blade replacement is the dominant recurring cost driver rather than motor failure [S3]. Selection of segment bond hardness, rim style, and wet-versus-dry operation determines whether a blade reaches the upper or lower end of that 80-300 h range [S1][S2].
Defining Marble Cutter Service Life and Wear Mechanism
Marble is a crystalline calcium-carbonate stone with Mohs hardness around 3, which forces diamond-blade manufacturers to use a harder bond matrix so the diamonds are exposed at a controlled rate rather than pulled out whole [S1]. Blade wear proceeds by three measurable mechanisms: segment abrasion (diamond pull-out and matrix erosion), core warping from heat cycling, and rim glazing where the bond polishes over the diamonds and cutting speed collapses [S1][S2].
Vacuum-brazed and electroplated manufacturing methods produce two distinct service profiles: vacuum-brazed blades retain a thicker diamond-bearing layer and tolerate repeated dressing, while electroplated thin-rim blades give cleaner cuts but reach end-of-life faster once the nickel coating is consumed [S1]. A blade should be retired when segment height falls below roughly 2 mm, when the cut surface shows progressive chipping, or when the steel core runs visibly out-of-plane above 0.5 mm of runout [S1].
Blade Type Comparison: Continuous Rim vs Segmented Rim vs Electroplated
Continuous-rim blades are built as a single uninterrupted diamond edge around the circumference, giving the smoothest, lowest-vibration cut on marble, and are the default choice for finished edges and tile work [S2]. Segmented-rim blades carry distinct gullets between diamond segments, which improve cooling and slurry evacuation and make them the standard for wet cutting of thicker marble slabs on bridge saws [S2].
Electroplated (nickel-bond) blades sit in a third category, built as a thin single-layer diamond coating suited to narrow kerfs and decorative cuts, but with the shortest service life of the three once the coating is consumed [S1]. The four-criteria comparison below summarises the trade-off:
Continuous-rim: edge quality high, cutting speed moderate, lifespan 80-200 h typical, best for dry or wet finish cuts on marble and limestone [S2]. Segmented-rim: edge quality moderate (slight chip risk), cutting speed high, lifespan 150-300 h with water cooling, best for wet slabbing on bridge saws [S2]. Electroplated: edge quality high, cutting speed high on soft stone, lifespan 20-60 h, best for decorative profiling where kerf width matters [S1].
Operating Variables That Cut Lifespan in Half
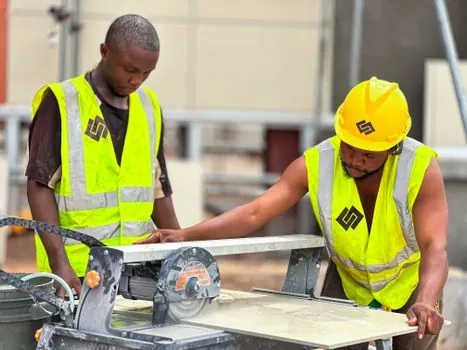
Dry cutting on marble is the single fastest blade killer, because marble's calcium-carbonate dust combines with frictional heat to glaze the bond matrix; Wandeli's selection guide notes that segmented blades used dry should be reserved for light-duty work and inspected after every pass [S2]. Forcing the cut, using a blade rated below the saw's RPM, or running a 1450 W handheld cutter without steady water feed can drop blade life from 200+ h to under 80 h on the same marble stock [S1][S3].
Bond hardness must be matched to marble's abrasiveness: a hard bond resists wear but glazes on soft stone, while a soft bond stays sharp but wears out prematurely on harder limestone or dolomitic marble variants [S1]. Material hardness varies, so a blade that runs 300 h on Carrara may run 120 h on a more abrasive crystalline marble from another quarry, and operators should track hours per square metre rather than rely on calendar time [S1][S2].
Inspection Schedule and Replacement Triggers
Segments should be visually checked every 4-6 hours of run time, with a straightedge across the rim to detect segment-set unevenness above roughly 0.3 mm, and a dial indicator on the steel core to catch runout before it cracks the bond [S1]. A blade that has dropped a segment, shows blue heat-discolouration on the core, or has lost more than 2 mm of segment height is past its service limit and must be replaced, not redressed [S1][S2].
On a 1450 W corded cutter such as the Tolsen 79533, the operator should also verify that the blade guard closes freely, the spindle lock holds, and the arbor matches the blade bore before every shift, since an undersized arbor on a worn blade is a common cause of dangerous shattering [S3]. For broader equipment longevity context outside the stone shop, cold milling machine drum replacement triggers follow a similar hours-based rather than date-based logic. Wet-cutting setups should also be paired with a working RCD on the supply, as specified in the tool manual's electrical-safety section [S3].
Cost-per-Cut Calculation and Sourcing
Premium continuous-rim blades with advanced bonding technologies consistently outlast cheaper alternatives, with manufacturer guidance indicating that higher-tier blades deliver longer life, cleaner cuts, and lower material waste from chipping [S2]. A practical cost-per-square-metre figure is obtained by dividing blade purchase price by (usable life in hours × average feed rate in m²/h), so a 150 h blade at 0.5 m²/h on marble yields 75 m² of cut, against 10-30 m² for an entry-level electroplated blade on the same material [S1][S2].
Buyers should request EN 13236 compliance documentation for diamond blades intended for the European market, and confirm the blade is rated for the RPM of the host machine, typically 11000-13000 RPM for a 110-125 mm handheld marble cutter [S3]. Storage matters as well: blades kept dry, in original packaging, and away from temperature swings above 40 °C retain bond integrity, while humidity-cycled blades have been observed to corrode at the segment-steel interface within months [S1].
Who Marble Cutters Are For, and Where They Are Not
Handheld marble cutters in the 1100-1500 W class, including 1450 W 220-240 V models like the Tolsen 79533, are specified for on-site trimming, sink cutouts, tile work, and small slab fabrication where portability outweighs the cut depth of a bridge saw [S3]. They are not the right tool for production stone-yards cutting full 2 m or 3 m slabs, where linear-guide gantry saws and dedicated bridge saws deliver straighter, deeper cuts at lower blade cost per metre [S2].
Within construction and finishing trades, marble cutters also overlap with other small power tools, and similar hours-based replacement thinking applies to items such as the rotary hammer bits and impact-driver consumables covered in this air impact wrench care routine for HVAC installers guide.
Track segment wear at every 20 hours of run time, log cuts per square metre on a per-job basis, and replace at the 2 mm segment-height threshold: this is the single highest-leverage habit for extending a marble cutter's economic life without sacrificing cut quality [S1][S2].
For component-level specifications, see crossed roller guide.