A structured marble cutter commissioning procedure runs four sequential gates, from site-readiness verification through signed acceptance, and the retention balance should not be released until each gate closes on paper.
For stone-processing shops, the two- to three-week window between truck arrival and first production part is where most latent defects get accepted. Treating that window as a formal protocol rather than a vendor demo is the single largest determinant of whether the machine performs the way it was sold [S1].
Scope: Which Machines the Protocol Covers
The protocol applies to handheld electric marble cutters, benchtop wet saws, bridge saws for slab processing, and CNC water-jet stone cutters, with the depth of each gate scaling to machine size and axis count [S5][S3]. Handheld units (typically 800-1,500 W class) require only a bench-test and a single test cut; bridge saws and CNC waterjets require full foundation, utility, axis-motion, and accuracy checks before any abrasive contact with stone [S1][S3].
For a marble cutter used in a fab shop, the same four-gate structure still applies, but the no-load mechanical run is shorter and the load-cut sample may be a single 600 mm tile rather than a full slab.
Gate 1: Site Readiness Before the Crate Opens
Foundation slab thickness and flatness must be confirmed against the machine's installation drawing before the rigger arrives, with anchor locations, isolation pads, and any grout or levelling compound specified in writing by the manufacturer [S1]. A bridge saw or CNC waterjet foundation typically demands a reinforced slab with deflection held within the maker's stated tolerance, because ways and ball screws amplify any concrete movement over time.
Electrical supply must match nameplate voltage, phase, and full-load current, with a lockable disconnect located where the maker specifies. Water supply must deliver the flow and pressure the cutter calls for: bridge saws and waterjets commonly need 2-4 bar at 10-20 L/min for the cooling/lubrication stream, while CNC waterjets need a separate high-pressure intensifier circuit rated to 380-420 MPa [S1][S3]. Slurry routing (trench, pit, or settling tank) must be in place before wet cutting begins, since a missing drain will halt testing the moment it is needed.
For waterjet installations, the abrasive delivery line, garnet hopper, and cutting-head nozzle must be on the pre-rigging checklist, because the high-pressure tubing, fittings, and abrasive metering are the items most often damaged in transit and least often inspected on arrival [S3].
Gate 2: Mechanical and Electrical No-Load Verification
With power locked out and tagged, the first powered checks are direction-of-rotation on every motor, guard interlock function on every door and shield, and emergency-stop response time measured end-to-end (typically under 1 second on a compliant rig) [S5]. On a CNC waterjet, axis travel is then run to soft limits and hard limits in both directions for X, Y, and Z, with any axis losing steps or hunting flagged before the cutting head ever sees stone [S3].
The diamond blade or abrasive disc is inspected for chips, cracks, and concentricity, then mounted to the maker's stated torque with a calibrated wrench. A handheld marble cutter should never be run dry beyond a few seconds for spin-up verification, because diamond segments overheat quickly without a water film and the bond can be ruined before the first real cut [S5].
Current draw on each phase is logged at no-load and compared to the nameplate, with a phase imbalance above roughly 10% typically indicating a supply or wiring issue rather than a machine fault. A useful cross-reference for this kind of pre-cut electrical audit is the same baseline-vs-drift discipline used in tensile testing machine acceptance, where a captured no-load number becomes the reference for every future service visit [S1].
Gate 3: Cold and Warm Test Cuts on Calibration Stock
Test cuts are run on calibration stock supplied by the buyer, not on the maker's demo slab, and the cut parameters (blade RPM, feed rate, water flow, abrasive flow rate, standoff distance for waterjet) are recorded for every pass [S1][S3]. For a bridge saw, a standard acceptance sample is a full 600 x 600 mm marble tile and a 600 x 600 mm granite tile, each cut to dimension and measured with calipers and a flatness gauge; for a waterjet, a 100 mm-thick slab with a programmed circle and a 45-degree bevel is the typical minimum [S3].
Acceptance criteria should be written into the purchase contract before delivery, with numbers not adjectives: typical written limits are dimensional tolerance +/- 0.5 mm over 600 mm, edge chip below 1.5 mm on marble and below 2.0 mm on granite, and perpendicularity under 0.3 mm per 100 mm of cut depth. Vague language like "acceptable cut quality" almost always turns into a scheduling argument later.
Waterjet-specific checks at this gate include high-pressure system stability under hold and cut pressure, tubing and fitting inspection at full pressure, abrasive delivery consistency, and cutting-head traverse along a programmed path with the abrasive stream on [S3]. Any pressure decay, garnet pulsation, or stream wandering is grounds to halt and call it a punch-list item, not a tuning issue.
Gate 4: Load-Cut Acceptance and Baseline Capture
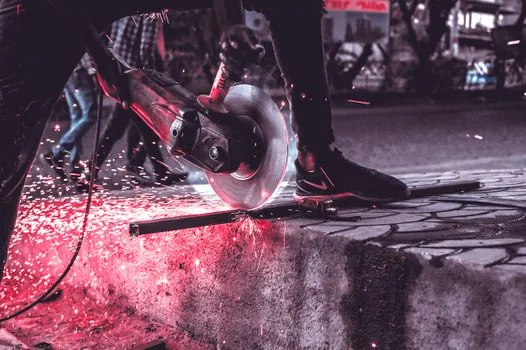
The load-cut gate is a sustained production run at the maker's rated throughput, typically 30-60 minutes of continuous cutting, with cycle time, surface finish, and consumable wear (blade wear land, garnet usage per metre of cut) all recorded [S1][S4]. This is also where the machine's as-installed baseline numbers are captured: spindle vibration in mm/s, axis repeatability in mm, hydraulic or pneumatic pressures at working temperature, and noise level in dB(A) at the operator station.
These numbers become the reference set every future service visit is compared against, which is the only way to tell degradation from a problem that shipped with the machine. A formal commissioning checklist normally partitions this work into verification (matches spec), testing (production-like cycles), and documentation (recorded proof of correct installation and safe operation) [S4].
Retention release should be tied to a signed punch list with a date next to every line item, not to a verbal "looks good." A useful pattern, also seen in construction machinery and equipment commissioning, is to hold the final 10-20% of payment until the punch list is closed, because once the money is gone, geometry problems become warranty claims, warranty claims become scheduling conversations, and scheduling conversations become weeks of degraded output [S1].
Common Failure Modes Caught at Commissioning
Misalignment between the bridge saw gantry and the table reference edge is the most common defect caught on a properly run acceptance test, and it is almost invisible during a vendor demo because the demo slab is chosen to mask it. Foundation bolts that were torqued before the grout cured, and water supply that drops below 1.5 bar under simultaneous cutting and table motion, are the next two most common late-discovered issues [S1].
On handheld and benchtop marble cutters, the dominant acceptance failure is blade runout above 0.1 mm, which shows up as chipping on marble edges even when the blade is new and the feed rate is conservative. Operators can cross-check this against the marble cutter working principle of diamond-blade contact, where runout and water flow are the two variables that govern edge chip [S5].
For waterjets, the recurring late-found problems are abrasive flow pulsation (caused by hopper bridging or worn metering nozzles), orifice-diamond misalignment that shows up only above 350 MPa, and Z-axis drift from a cutting head that was not re-squared after rigging. Each of these is detectable in a 30-minute Gate 3 test if the acceptance protocol requires a 45-degree bevel and a programmed circle rather than a straight line [S3].
Training, Spares, and the Documentation Hand-Off
Operator training should start at the builder's runoff stage, not at the buyer's site, so operators are already familiar with the HMI, interlocks, and fault-recovery sequence before the machine is under their own site's utilities [S4]. A documented training record, signed by both the maker's technician and the buyer's operator, is the most reliable evidence later that a fault was driven by the process, not by the machine.
The spares list agreed at commissioning should be a wear-rated list, not a generic "consumables" entry, with the maker's expected life stated in hours or metres of cut for each item. For a bridge saw, the typical minimum starter set is one diamond blade, one set of drive belts, and the maker-recommended grease and hydraulic fluid in unopened containers; for a waterjet, it is one orifice/diamond pair, one set of high-pressure seals, and a 25 kg bag of the same garnet grade used during commissioning [S4].
The final hand-off folder should include the as-built electrical schematic, the hydraulic or pneumatic schematic if any, the parameter file backup from the CNC, the baseline readings from Gate 4, the signed punch list, and the contact-and-escalation list. Anything not in that folder tends to be missing the first time the machine is down at 02:00.
Trackable signals over the next quarter: whether the maker publishes a new written acceptance-protocol template alongside the next CNC waterjet or bridge saw model launch, and whether more procurement contracts in 2026 are starting to attach specific dimensional and edge-chip limits rather than the older "to be agreed" clauses, since the latter is the single largest source of post-commissioning disputes flagged in the field literature [S1].