The flight pitch-to-diameter ratio (P/D) is the single geometric parameter that most directly controls screw conveyor capacity, inclination behaviour, and material agitation. Standard industrial practice defines four ratio bands: standard (P = D), short (P = 2/3 D), half (P = 1/2 D), and long (P = 1.5 D), with the screw conveyor component guide in current use mapping each band to a specific application envelope [S1][S2].
Selection is not optional: the same screw running horizontally, on a 15-degree incline, and vertically requires three different pitch ratios to stay inside the operating envelope, because capacity decreases as the limiting angle on the flight face changes with both friction coefficient and P/D [S8]. CEMA-type sizing methods in the US and equivalent SHAPA-type methods in the UK still treat P/D as a primary design variable alongside diameter, speed, and loading ratio [S4].
Standard Pitch P = D: Horizontal and Low-Incline Baseline
Standard pitch, single flight screws have outside diameter equal to pitch and are the most common screw type used for horizontal screw conveyors and inclines up to 10 degrees [S1]. Kase Conveyors' engineering guide treats pitch equal to screw diameter as the reference case, suitable for a wide range of materials in most conventional applications [S2]. The standard P/D = 1 ratio produces the highest volumetric capacity per revolution at a given diameter, which is why it dominates horizontal bulk-solids conveying where inclination drag and flushing are not the controlling concern.
For free-flowing materials at zero incline, capacity scales with D cubed, screw speed N, and loading ratio alpha, with typical maximum alpha values of 0.40 to 0.45 for free-flowing solids and 0.12 to 0.15 for non-free-flowing solids in the PowderProcess design procedure [S4]. Inclination correction factor C drops from 1.00 at 0 degrees to 0.90 at 5 degrees, 0.80 at 10 degrees, 0.70 at 15 degrees, and 0.65 at 20 degrees, so a 20-degree incline with a standard pitch screw is derated to roughly 65 percent of the horizontal figure before any other adjustment [S4].
Short Pitch P = 2/3 D and Half Pitch P = 1/2 D: Incline and Vertical Duty
Short pitch, single flight screws have the pitch reduced to 2/3 of the diameter and are most commonly used in inclined and vertical screw conveyor applications; the shorter pitch retards flushing of materials which fluidize [S1][S2]. Half pitch, single flight screws drop further to P = 1/2 D and are commonly used in inclined and vertical applications, screw feeders, and handling extremely fluid materials where flushing is a dominant failure mode [S1][S2]. Reducing P/D shortens the axial advance per revolution, which lowers the fluidising tendency on the flight face and keeps the bulk bed from riding up the flight wall on a slope or in a vertical casing.
Stainless-steel tube/pipe screw conveyors in food, pharma, and chemical service often run at 15 to 30 degrees with short pitch to balance capacity against residue carry-back. Per published CEMA-aligned design tables, the inclined-screw correction factor falls below 0.80 once inclination passes 10 degrees, so a 0.1 m diameter standard pitch screw carrying 800 kg/m3 free-flowing sugar at 0 degrees delivers 17 kg/h per rpm, and the same screw on a 15-degree incline must either drop pitch, increase diameter, or increase speed to hold the 3500 kg/h design point [S4].
Long Pitch P = 1.5 D: Agitation and Free-Flowing Rapid Transfer
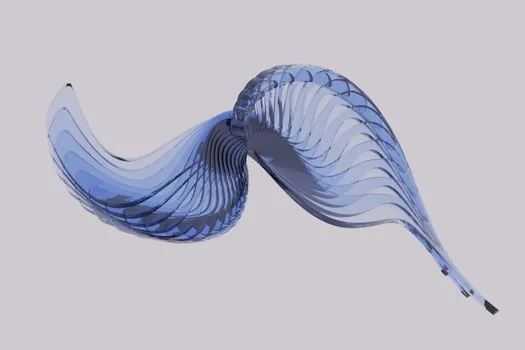
Long pitch screws carry pitch equal to 1.5 diameters, described as useful for agitating fluid materials or for rapid movement of very free-flowing materials [S2]. Screw Conveyor Parts Ltd defines long pitch as more than full pitch, usually 1.5x the screw diameter, and ties it to applications where axial advance per revolution and throughput per RPM matter more than bed stability [S5]. Long pitch should not be used on inclines above roughly 10 degrees or for materials with cohesive or fibrous character, because the long axial advance per revolution promotes flushing of the bed on the flight face and back-mixing in the trough.
Long pitch also shows up in mixer-dryer and aeration screws where the goal is gentle tumbling rather than positive displacement, but for positive-conveying service the standard ratio dominates because it gives the highest coupling coefficient between screw rotation and material translation along the trough axis.
Variable Pitch, Tapered, and Ribbon: Feeder and Sticky-Material Variants
Variable pitch, single flight screws have increasing pitch with every flight and are used in screw feeders to provide uniform withdrawal of free-flowing bulk materials from hoppers, bins, or silos [S1]. Screw Conveyor Parts frames it as a flooded inlet problem: the inlet end uses a short pitch to meter material, then a larger pitch conveys it along the screw length, which prevents a flooded inlet from packing the trough and over-torquing the drive [S5]. Tapered flight screws differ by holding pitch constant and growing the flight outside diameter from 2/3 D to full D along the inlet, producing a similar uniform draw-down effect for lumpy materials and often substituting economically for variable pitch [S2][S6].
Ribbon flight screws leave an open space between the flight helix and the central pipe to minimise collection and buildup of viscous and sticky bulk materials, and the standard pitch ratio still applies; only the flight surface is interrupted [S1]. Mass flow screws combine an internal cone with variable pitch to give increasing volume with every flight, a common solution for hard-to-meter cohesive powders discharging from a silo [S1].
Pitch-to-Diameter Ratio Selection: A Decision Comparison
The four standard P/D bands are best selected by working from incline angle, flowability, and feeder-versus-conveyor duty, not from a single table. KWS Manufacturing and Kase Conveyors publish the same canonical bands, and PowderProcess bundles them into a single selection step inside its design procedure [S1][S2][S4].
Comparison across the main options on four decision criteria, drawn from KWS, Kase, and Screw Conveyor Parts: (1) P/D = 1 standard, suited to horizontal and inclines up to 10 degrees, all material classes, gives the highest capacity per RPM, default for general-purpose conveyors; (2) P/D = 2/3 short, suited to inclined and vertical, particularly fluidising materials, gives lower capacity per RPM but resists flushing, default for incline service above 10 degrees; (3) P/D = 1/2 half, suited to vertical, screw feeders, and extremely fluid materials, lowest capacity per RPM but the most stable bed in steep or vertical runs; (4) P/D = 1.5 long, suited only to near-horizontal agitation of very free-flowing materials, gives the highest throughput per RPM on free-flowing solids but is not a general-purpose choice [S1][S2][S5].
Practical caveat: the limiting angle that defines whether a given P/D still works on an incline depends on the coefficient of sliding friction of the bulk solid against the flight face as well as the pitch-to-diameter ratio itself, so two plants running the same nominal P/D with different materials can land in different application envelopes [S8]. When in doubt on an inclined service, drop to short or half pitch before increasing motor power, because the inclination correction factor derates capacity faster than the motor can typically recover it [S4].
Fabrication Geometry: Pitch, Blank Diameter, and Pattern Development
For fabricated flighting, the relevant P/D inputs are screw outside diameter D, pipe inside diameter d, pitch P, and flight thickness T, with the development radii R1 and R2 and the radial cut angle beta calculated from those inputs [S3]. LetsFab's screw flight calculator spells out the inputs needed to produce a flat pattern or blank plate layout: D is the outside diameter of the finished flight, d is the inside diameter that fits over the central pipe, P is the helical pitch, and T only matters for weight, not for the flat layout itself [S3].
For carbon-steel sectional flights pressed one pitch at a time, and for helicoid flights formed from coil stock in one continuous helix, the pitch-to-diameter ratio is set at the forming stage and is not adjustable after manufacture without re-rolling; for paddle and cut-and-folded flight variants, the underlying pitch is still one of the four canonical ratios, and the cut or paddle geometry is added on top of that ratio [S1][S2].
For loadout and bin-discharge service using screw conveyors integrated with bucket elevators, the matching chain or belt elevator selection on the discharge side typically references the upstream screw's pitch family to keep throughput aligned, and a related selection reference on bucket-elevator chain types is available at chain versus bush versus plate bucket elevator selection. For mechanical-drive interfaces on the screw end (couplings, bushings, taper bush sizing), the screw conveyor component spec typically cross-references a standard taper bush series, and a sizing reference for that interface is at taper bush bore range sizing.
Limitations, Failure Modes, and Sourcing Anchors
Published P/D guidance is consistent across KWS, Kase, Screw Conveyor Parts, and PowderProcess, which makes the canonical bands (1, 2/3, 1/2, 1.5) the safest baseline for a spec; deviations outside those bands should be tied to a numerical or pilot validation [S1][S2][S4][S5]. The 2024 ACS Energy Fuels paper on numerical validation of screw conveyor design methods treats pitch, radius, incline, rotation speed, and bulk density as the primary degrees of freedom in a throughput model, which is a useful anchor for any project proposing a non-standard P/D [S7].
Trackable signals for the next design cycle: monitor CEMA and SHAPA guidance updates for any change to inclination-correction factors C at 5-degree increments, and watch for revisions to the canonical pitch band table (currently 2/3 D and 1.5 D as the short and long extremes) [S4]. On the materials side, the friction-coefficient dependency flagged by ScienceDirect's screw conveyor overview means that any change in bulk-solid specification, especially a switch to a lower-friction or higher-fluidity product, should trigger a re-check of the P/D band before the motor and gearbox are re-specified [S8].
Spec-level background on the components involved: ball screw, and lead screw.