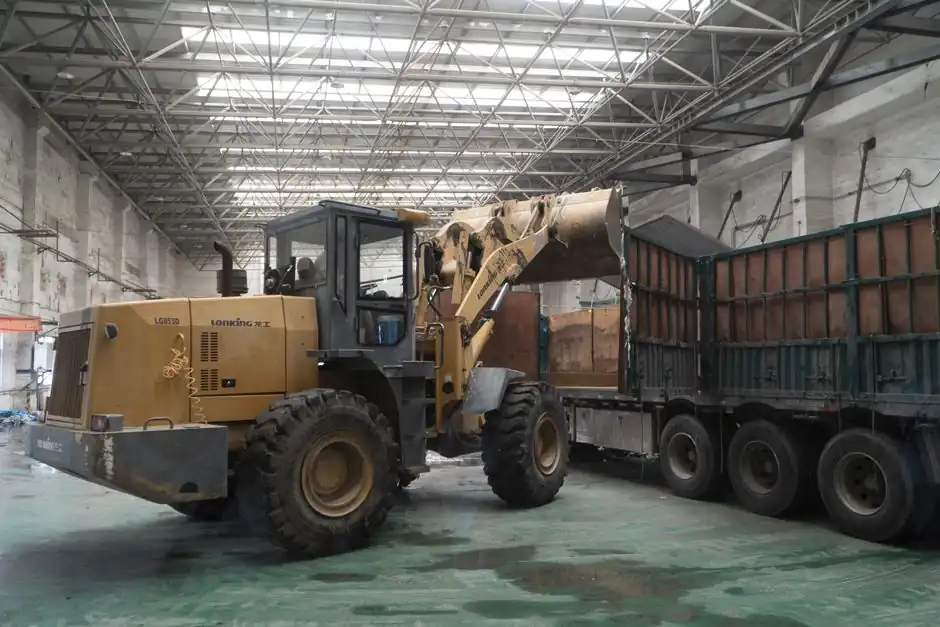
Industrial shock absorbers convert kinetic and drive energy into heat, and the four datasets that drive every correct selection are effective mass, impact velocity, propelling force, and hourly cycle rate, per ACE Controls guidance published 2026-06-26 [S4].
Material handling covers a wide load profile, from 1 kg conveyor stops to 50 t bridge-crane buffers, so a single catalogue number rarely covers a facility. Misumi's 2026-01-08 industrial buyer's guide and SMC's RB/RBQ/RBL series catalog both anchor selection on the same three energies, kinetic E1, thrust E2, and absorbed E = E1 + E2 [S1][S2].
The Four Datasets That Decide Every Selection
Effective mass is the total inertia arriving at the absorber face, including the primary payload, grippers and fixtures, the moving carriage, and the cylinder rod, with rotary linkages reduced to an equivalent linear mass at the point of impact [S4]. A common pitfall is weighing only the payload and missing the drive-side inertia, which can swing the energy calculation by a factor of 1.3 or more on a cable-slung crane [S3].
Impact velocity must be the velocity at the exact millimetre of contact, not the average stroke velocity, and pneumatic cylinders are the classic trap because they accelerate through the full stroke and peak right before end-of-travel [S4]. Taylor Devices' design guide formalises this: V = 2 × average cylinder velocity for air-driven systems, V = 1.5 × average for hydraulic, and V² = 2 × a × distance for known-acceleration profiles [S3].
Propelling force is the work-energy the drive keeps adding while the absorber strokes, so pneumatic sizing is bore area × supply pressure, electric/hydraulic sizing is motor torque × gearbox and lead-screw efficiency, and gravity on an incline is m·g·sin(θ) [S4]. If Fd exceeds the unit's rated propelling force, step up one size and re-solve Ew, because the seal stack will not survive a stalled piston [S5].
Kinetic, Work, and Total Energy: The Three Numbers
For a linear horizontal system, kinetic energy Ek (in-lb) = (W/722) · V² where W is the moving weight in pounds and V is in inches per second; the same equation is the per-cycle energy the absorber must convert to heat [S5]. The work-energy term Ew = Fd · S adds the drive's contribution over the full stroke S (in), and the per-cycle total is Et = Ek + Ew, divided by the number of parallel absorbers if more than one shares the load [S5].
For overhead cranes, Taylor Devices defines an effective weight WE that captures the sling-shot effect: bridge buffer WE = 1.3 · (0.5 · bridge + trolley) or 0.5 · (bridge + trolley + lifted load), whichever is greater, and trolley buffer WE = 1.3 · (0.5 · trolley) or 0.5 · (trolley + lifted load) [S3]. Sizing to average mass instead of WE is the documented cause of premature buffer failures on container-handling cranes.
SMC's selection flow for the RB series follows the same arithmetic with metric units: E1 = 0.5 · m · v², E2 = F1 · S, and the corresponding impact mass Me = 2(E1+E2) / v² is matched against each model's maximum, so RB0604 with a 3 kg Me ceiling satisfies a worked 1 kg / 0.5 m/s example at 30 cycles per minute [S2].
Fixed vs Adjustable vs Self-Compensating
Fixed- orifice units are tuned for one load/velocity window, ship tamper-proof, and cost the least, so they are the right call when impact parameters are predetermined and stable, such as a single-product conveyor stop [S1]. Adjustable units use an orifice knob, a self-regulating valve, or an electronic/semi-active loop to track varying loads and speeds, and are the default for docks, cranes, and mixed-SKU pallet handling [S1][S7].
Self-compensating hydraulic designs, including SMC's RB family and Enidine's heavy-duty range, are built to absorb a wide speed-load envelope without manual re-tuning, which removes the field-adjustment error mode on dampening curves and is well suited to packaging lines and rotating-shaft stops [S2][S5]. Single-orifice units peak force at the start of stroke (where impact velocity is highest) and package high energy absorption into short bodies, while multi-orifice units spread the damping force more evenly across the stroke and run cooler at high cycle rates [S1].
For a comparison, the three options line up against the main selection criteria as follows: fixed units win on cost, tamper-proofing, and repeatability, but lose on flexibility; adjustable units win on flexibility and are competitive on cost, but introduce a tuning step; self-compensating units win on uptime and low-maintenance operation, but cost more per cycle of energy absorbed and typically weigh more for the same rating [S1][S5].
Cycle Rate, Heat, and the 85% / 30% Rules
Once Et is known, multiply by cycles per hour to get the hourly thermal load Etc = Et · C, and the unit's rated hourly capacity must exceed it; otherwise the shock will run hot, hydraulic viscosity will drop, and internal seals will fail [S5]. A practical baseline is 85% efficiency for typical industrial shocks, meaning the catalogue's energy-per-cycle figure already accounts for some loss, but you still need headroom [S5].
Taylor Devices' hard rule is that for cyclic rates above 240 per hour you must apply a 30% safety factor on energy capacity, and for sustained heat loads beyond that you typically need a side-mounted oil pocket, an air/oil cooling loop, or a larger body to grow the radiating surface area [S3][S4]. Sorbothane and other viscoelastic polymers sit on the other end of the duty spectrum: high hysteresis, low cycle rate, and best for isolation rather than high-energy stopping [S8].
Quoting the Taylor Devices design guide directly, "An improperly sized shock absorber can be a safety hazard", which is why every selection path ends with a checklist on Et per cycle, Etc per hour, propelling force, and available stroke before a part number is released [S3].
Material Handling Use Cases and What Spec Wins
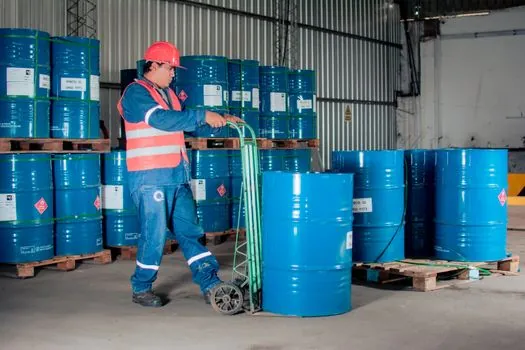
Dock equipment and cranes tend to demand adjustable or self-compensating units with high effective-weight ratings and bridge/trolley buffer geometry, because the lifted load swings and overspeed conditions change WE on every cycle [S3][S7]. For conveyor transfers and pallet stops the energy per cycle is lower but the cycle rate is high, so a multi-orifice or self-compensating unit with side-port cooling is usually the correct trade-off [S1][S9].
Roller-supported moving masses are a documented pain point where standard catalogues under-size because the rolling contact adds friction variability, and Shockbuffer's medium industrial line is built specifically for that profile with energy ratings matched to in-line conveyor decelerations [S9]. The four-dataset method (mass, impact velocity, propelling force, cycle rate) covers all of these cases once the per-cycle Et and per-hour Etc are both inside the catalogue envelope [S4].
Limitations, Failure Modes, and What the Method Does Not Catch
The four-dataset method assumes a linear deceleration profile; if the application requires a soft-stop, hard-stop, or progressive curve, the catalogue's "linear" rating understates the peak force at the start of stroke and the unit must be de-rated accordingly [S4]. It also assumes the absorber is mounted within the published alignment tolerance (SMC quotes a 5° allowable eccentric angle for the RB/RBQ family), and side-loads outside that window introduce rod wear that the sizing math cannot see [S2].
High-temperature environments near ovens, foundry lines, or paint booths lower hydraulic viscosity and shift the damping curve, so the same unit that works at 25 °C will feel softer at 60 °C, and the hourly capacity Etc must be re-derived for the real ambient [S2][S4]. The method is also silent on corrosion: dock and outdoor crane buffers need plated rods and marine-grade seals or the service life is set by rust, not by the energy math [S1].
Verification, Standards, and Sourcing Trail
Every selection should land on a manufacturer datasheet that lists stroke, usable velocity range, maximum energy per cycle, maximum propelling force, and hourly thermal capacity, then compare those five numbers against the application's Et, Etc, V, Fd, and S [S5]. A simple audit: Et (per cycle) must be less than the rated energy per cycle, Etc must be less than the rated hourly capacity, V must sit inside the usable velocity window, Fd must be below the maximum propelling force, and the catalogue stroke must be at least the calculated S with a 5 to 10 mm safety margin [S3][S5].
Trackable signals worth watching over the next two quarters: ACE Controls' sizing calculator updates for the four-dataset flow, SMC's next RB/RBQ catalogue revision covering the M6 to M27 thread range, and any new self-compensating releases aimed at conveyor and roller-deceleration duties from the medium-industrial segment [S1][S2][S4][S9]. Engineers specifying shock absorbers into a material handling line should also bookmark the broader storage handling reference so dock and warehouse stops are picked from the same efficiency baseline.
Background reading: Acetylene vs Propane for Oxy-Fuel Cutting: Speed, Cost, and Spec Matchup.